CN201002181Y - Welding jig for prismatic batteries - Google Patents
Welding jig for prismatic batteries Download PDFInfo
- Publication number
- CN201002181Y CN201002181Y CNU2006201664621U CN200620166462U CN201002181Y CN 201002181 Y CN201002181 Y CN 201002181Y CN U2006201664621 U CNU2006201664621 U CN U2006201664621U CN 200620166462 U CN200620166462 U CN 200620166462U CN 201002181 Y CN201002181 Y CN 201002181Y
- Authority
- CN
- China
- Prior art keywords
- support frame
- cam
- push rod
- battery
- guide
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Landscapes
- Sealing Battery Cases Or Jackets (AREA)
Abstract
本实用新型提供一种方形电池的焊接夹具,用于在对方形电池的外壳进行焊接时将电池准确牢固地定位,充分保证电池的焊接强度和密封性能。该方形电池的焊接夹具包括支撑框架、推杆、导杆和凸轮,其中支撑框架具有上下左右四个侧边,这四个侧边围成一个空间,且相对的侧边彼此平行;推杆平行于上下侧边设置在支撑框架中,推杆的两端分别可上下滑动地设置在支撑框架的左右侧边上,推杆中具有垂直设置的导孔;导杆的一端固定在支撑框架的上侧边或下侧边上,另一端插入到所述导孔中;凸轮可转动地铰接在支撑框架的上侧边的中间位置,凸轮的凸轮面与推杆的上表面可滑动地接触。通过转动凸轮,可以驱动推杆向下移动,从而将电池准确、牢固地定位。
The utility model provides a welding fixture for a square battery, which is used for accurately and firmly positioning the battery when welding the shell of the square battery, and fully guarantees the welding strength and sealing performance of the battery. The welding fixture of the square battery includes a support frame, a push rod, a guide rod and a cam, wherein the support frame has four sides, up, down, left, and right, and these four sides form a space, and the opposite sides are parallel to each other; the push rod is parallel to each other. The upper and lower sides are arranged in the support frame, and the two ends of the push rod are respectively arranged on the left and right sides of the support frame to slide up and down, and the push rod has a vertical guide hole; one end of the guide rod is fixed on the top of the support frame. On the side or lower side, the other end is inserted into the guide hole; the cam is rotatably hinged in the middle of the upper side of the support frame, and the cam surface of the cam is in slidable contact with the upper surface of the push rod. By turning the cam, the push rod can be driven to move down, so that the battery can be positioned accurately and firmly.
Description
技术领域technical field
本实用新型涉及在电池焊接过程中使用的电池夹具,具体涉及一种方形电池的焊接夹具。The utility model relates to a battery clamp used in the battery welding process, in particular to a square battery welding clamp.
背景技术Background technique
随着社会对环保要求的提高,安全、无污染且容量高的锂离子电池成为目前理想的新一代能源。它被广泛应用于手机、PDA、EV、HEV等领域。一般锂离子电池包括由正负极片和隔膜组成的极芯,用于封装极芯的电池外壳,以及注于外壳中的电解液。对于小型电池的外壳,由于体积较小,外壳和底盖可以在外壳成形过程中与外壳拉伸成一体结构,在封装极芯时,只需焊接盖板就可以了。但对于中大容量和中大功率的锂离子电池外壳来说,由于其体积较大,外壳和底盖需要经过一道焊接工序连接在一起。With the improvement of society's environmental protection requirements, safe, pollution-free and high-capacity lithium-ion batteries have become an ideal new generation of energy. It is widely used in mobile phones, PDAs, EVs, HEVs and other fields. A general lithium-ion battery includes a pole core composed of positive and negative electrodes and a separator, a battery case for encapsulating the pole core, and an electrolyte injected into the case. For the case of a small battery, due to its small size, the case and bottom cover can be stretched into an integral structure with the case during the forming process of the case. When packaging the pole core, only the cover plate needs to be welded. However, for lithium-ion battery casings with medium and high capacity and high power, due to their large size, the casing and bottom cover need to be connected together through a welding process.
在现有技术中,电池中外壳和底盖以及外壳和盖板的焊接通常由激光焊接机来完成。激光焊接机是应用高能脉冲激光对物件进行焊接,激光脉冲的高能量、高密度可使焊接平整、焊缝宽度小以及热影响区小,能完成传统工艺无法实现的精密焊接。另外激光焊接效率高、效果好、操作简单方便,适用于各种材料的平面直线、圆弧及任意轨迹的焊接。因此激光焊接广泛应用于钢/铝壳电池外壳和盖板及底板的焊接生产中。通过激光焊接机对电池外壳和底盖以及外壳和盖板进行焊接已经记载在多篇专利文献中,例如,CN2573143 Y,CN 2614834 Y,CN 2614835 Y等等。In the prior art, the welding of the casing and the bottom cover and the casing and the cover plate in the battery is usually completed by a laser welding machine. Laser welding machine uses high-energy pulse laser to weld objects. The high energy and high density of laser pulse can make the welding smooth, the weld width is small and the heat-affected zone is small, and it can complete the precision welding that cannot be realized by traditional technology. In addition, laser welding has high efficiency, good effect, simple and convenient operation, and is suitable for welding of plane straight lines, arcs and arbitrary trajectories of various materials. Therefore, laser welding is widely used in the welding production of steel/aluminum battery case, cover plate and bottom plate. Welding the battery case and bottom cover and case and cover plate by laser welding machine has been recorded in many patent documents, for example, CN2573143 Y, CN 2614834 Y, CN 2614835 Y or the like.
然而,由于钢/铝壳电池的外壳壁厚往往很小,如果在激光焊接中稍有偏差,就会造成焊接强度不够或密封性能受到影响,造成电池漏液等安全问题,所以为了保证电池焊接的强度和密封性能,客观上对固定电池外壳的激光焊接夹具的定位精度提出了较高要求。However, since the shell wall thickness of steel/aluminum shell batteries is often very small, if there is a slight deviation in laser welding, the welding strength will be insufficient or the sealing performance will be affected, causing safety problems such as battery leakage, so in order to ensure battery welding The strength and sealing performance objectively put forward higher requirements for the positioning accuracy of the laser welding jig that fixes the battery case.
实用新型内容Utility model content
本实用新型的目的是提供一种方形电池的焊接夹具,用于在对方形电池的外壳进行焊接时将电池准确、牢固地定位,以充分保证电池的焊接强度和密封性能。The purpose of the utility model is to provide a welding jig for a square battery, which is used to accurately and firmly position the battery when welding the shell of the square battery, so as to fully ensure the welding strength and sealing performance of the battery.
本实用新型所提供的方形电池的焊接夹具包括支撑框架、推杆、一对导杆和凸轮,其中:支撑框架具有上下左右四个侧边,这四个侧边围成一个空间,且相对的侧边彼此平行;推杆平行于上下侧边设置在支撑框架中,推杆的两端分别可上下滑动地设置在支撑框架的左右侧边上,推杆中具有垂直设置的导孔;导杆的一端固定在支撑框架的上侧边或者下侧边上,另一端插入到所述导孔中;凸轮可转动地铰接在支撑框架的上侧边的中间位置,凸轮的凸轮面与推杆的上表面可滑动地接触。The welding fixture of the square battery provided by the utility model includes a support frame, a push rod, a pair of guide rods and a cam, wherein: the support frame has four sides of up and down, left and right, and these four sides enclose a space, and the relative The sides are parallel to each other; the push rod is arranged in the support frame parallel to the upper and lower sides, and the two ends of the push rod are respectively arranged on the left and right sides of the support frame to slide up and down, and the push rod has a vertical guide hole; the guide rod One end is fixed on the upper or lower side of the support frame, and the other end is inserted into the guide hole; the cam is rotatably hinged at the middle position of the upper side of the support frame, and the cam surface of the cam and the push rod The upper surface is in slidable contact.
在焊接电池外壳时,首先将电池放置到支撑框架的空间内,然后通过使凸轮相对于支撑框架的上侧边转动,通过凸轮的凸轮面驱动推杆垂直向下移动,从而通过推杆将电池牢牢固定住,以便进行精确的激光焊接。在转动凸轮时,凸轮面沿着推杆的上表面滑动,在凸轮面的远轴点滑动到推杆的上表面上时,凸轮锁死,推杆向下移动最远距离,从而将电池牢固且稳定地压在支撑框架中,即电池被固定在支撑框架的下侧边与推杆之间。When welding the battery casing, the battery is first placed in the space of the support frame, and then the cam is rotated relative to the upper side of the support frame, and the cam surface of the cam drives the push rod to move vertically downwards, so that the battery is moved by the push rod Holds securely for precise laser welding. When the cam is rotated, the cam surface slides along the upper surface of the push rod, and when the abaxial point of the cam surface slides onto the upper surface of the push rod, the cam locks and the push rod moves down the farthest distance, thereby firmly holding the battery And it is stably pressed in the support frame, that is, the battery is fixed between the lower side of the support frame and the push rod.
因此,通过本实用新型的技术方案,在对方形电池的外壳进行焊接时可以方便地将电池准确、牢固地定位,从而能够充分保证电池的焊接强度和密封性能。Therefore, through the technical solution of the utility model, the battery can be conveniently and accurately and firmly positioned when welding the casing of the prismatic battery, thereby fully ensuring the welding strength and sealing performance of the battery.
附图说明Description of drawings
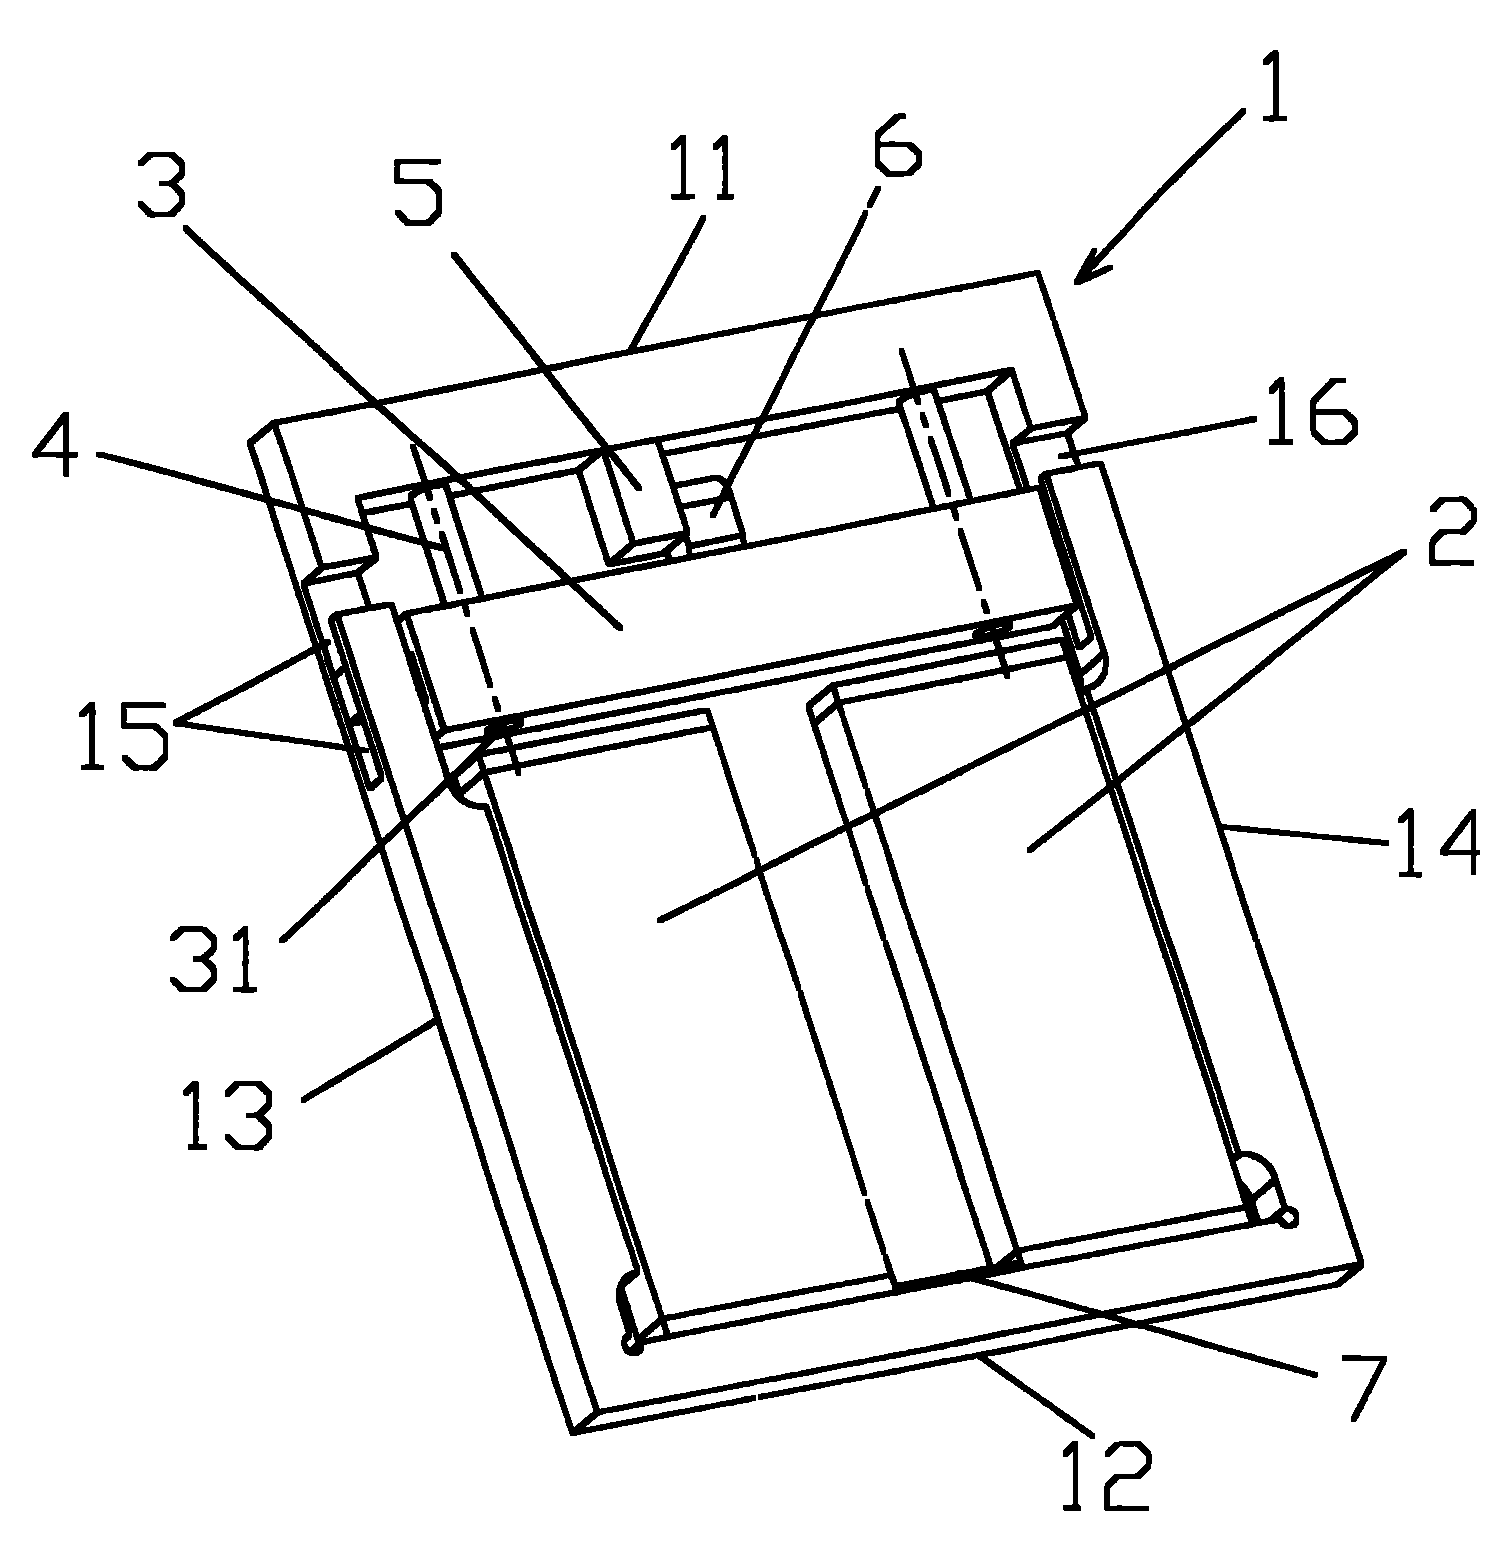
图1是本实用新型的方向电池焊接夹具的典型实施方式的立体图;Fig. 1 is a perspective view of a typical embodiment of a directional battery welding jig of the present invention;
图2是图1中支撑框架的结构图;Fig. 2 is a structural diagram of the support frame in Fig. 1;
图3是图1中凸轮和凸轮支柱的分解立体图;Fig. 3 is an exploded perspective view of the cam and the cam support in Fig. 1;
图4是图1中凸轮的工作示意图。Fig. 4 is a working diagram of the cam in Fig. 1 .
附图说明Description of drawings
下面参照附图详细描述本实用新型。Describe the utility model in detail below with reference to accompanying drawing.
如图1所示,根据本实用新型的一种典型实施方式,提供一种方形电池的焊接夹具,该夹具包括支撑框架1、推杆3、一对导杆4和凸轮6,其中:支撑框架1具有上下左右四个侧边11、12、13、14,这四个侧边围成一个空间,且相对的侧边11和12以及13和14彼此平行;推杆3平行于上下侧边11和12设置在支撑框架1中,推杆3的两端分别可上下滑动地设置在支撑框架1的左右侧边1 3、14上,推杆3中具有垂直设置的导孔31;导杆4的一端固定在支撑框架1的上侧边11或下侧边12上,另一端插入到所述导孔31中;凸轮6可转动地铰接在支撑框架1的上侧边11的中间位置,凸轮6的凸轮面61与推杆3的上表面可滑动地接触。As shown in Figure 1, according to a typical embodiment of the present invention, a welding fixture for a square battery is provided, the fixture includes a
支撑框架1优选为一体式结构,由铜、不锈钢、钢、铝合金等具有一定强度的材料制造,因此力学性能好,在长时间使用后不会发生由于变形而导致电池定位不准,造成焊接轨迹的偏移,因而对电池具有较高的定位精度。在使用时,电池2定位在支撑框架1中由支撑框架的四个侧边围成的空间中,更具体地是定位在支撑框架1的左右侧边和下侧边与推杆3的下表面之间的空间中,从而通过推杆3的上下移动,可以夹持或者松开电池2。The
作为例子,如图1所示,可以同时将两个电池2放置到支撑框架1的空间中,对电池外壳进行激光焊接。但是,本实用新型不限于此。本领域技术人员容易理解,通过对支撑框架1或者支撑框架1中的空间进行简单的尺寸修改,可以将一个电池,或者三个或者更多个电池同时放置到支撑框架的空间中,以对电池外壳进行激光焊接。As an example, as shown in FIG. 1 , two batteries 2 can be placed in the space of the supporting
在图1所示的将两个电池同时放置到支撑框架1的空间中时,优选地可以在支撑框架1的下侧边12的内侧的中间位置设置一个凸台7(详细图示见图2)。通过这个凸台7,在将两个电池2和待焊接的电池底盖或者盖板放置到空间中时,可以以这个凸台7作为基准,准确定位这两个电池和电池底盖或者盖板。在需要焊接电池外壳和底盖或者电池外壳和盖板时,将底盖或者盖板放置在凸台7的两侧,然后将电池2放置到底盖或者盖板上,准确定位。优选地,所述凸台7的高度稍微小于底盖或者盖板的厚度。如果凸台7与底盖或者盖板平齐,或者甚至高于底盖或者盖板,则当激光经过凸台与底盖或者盖板接触位置的时候,有可能会出现炸火现象,从而存在安全隐患。When two batteries are simultaneously placed in the space of the
另外,本领域技术人员应当理解,上述凸台7的布置仅仅是一种优选的实施例,在本实用新型的保护范围之内可以根据支撑框架1中放置的电池2的数量等因素对凸台7的布置进行适应性修改。例如,在一个支撑框架1中放置三个或者更多个电池2的情况下,则可以在相邻的每两个电池2之间设置一个凸台7,从而可以对每个需要焊接的电池底盖或者盖板进行准确定位。In addition, those skilled in the art should understand that the arrangement of the above-mentioned boss 7 is only a preferred embodiment, and within the protection scope of the present utility model, the arrangement of the boss 7 can be adjusted according to the number of batteries 2 placed in the
如图1和图2所示,为了使推杆3能够在支撑框架1中垂直上下移动,可以在支撑框架1的左右侧边13和14上设置导槽15和16,将推杆3的左右两端分别设置在导槽15和16内,从而能够沿着导槽15和16上下移动。由此,即可实现推杆3相对于支撑框架1的垂直移动。本领域技术人员应当理解,这种结构仅仅是本实用新型的一种实施例,但是本实用新型并不限于这种特定的结构。通过现有技术中的其它结构,同样可以实现推杆3在支撑框架1中的垂直上下移动。例如,可以将支撑框架1的左右侧边13和14的全部或者一部分制成导轨或者导柱,并相应地将推杆3的两端设置成与之配合的导槽或导向环;或者将支撑框架1的左右侧边13和14的全部或者一部分的内表面设置成特定的形状如倒T形,同时将推杆3的两端设置成与之匹配的形状,等等,都能够实现推杆3相对于支撑框架1的垂直(即上下)移动。As shown in Figures 1 and 2, in order to enable the
导杆4的作用是为了引导推杆3在支撑框架1中作上下移动。导杆4的形状可以是圆柱形、方形、三角形等等,优选为圆柱形。所述推杆3中的导孔31的形状与导杆4一致,相互配合。The function of the
如图1和图2所示,作为一种优选的实施例,所述导杆4包括一端固定在支撑框架1的上侧边11的左右两侧的一对导杆,所述推杆3中的导孔31则包括与该一对导杆相对应的一对导孔。一对导杆4的下端分别插入到一对导孔31中,以便引导推杆3在支撑框架1中的上下移动。As shown in Figures 1 and 2, as a preferred embodiment, the
本领域技术人员应当理解,上述导杆4的结构仅仅是一种优选的实施例,在本实用新型的保护范围之内可以对导杆4进行各种修改。例如,作为一种例子,可以将导杆4设置在推杆3与支撑框架1的下侧边12之间,并位于左右方向的中间位置。或者,在一个支撑框架1中放置三个或者更多个电池2的情况下,则还可以在相邻的每两个电池2之间设置一根导杆4。因此,本实用新型对导杆4的具体结构和设置方式不作特别限定,只要导杆4能够实现引导推杆3相对于支撑框架1垂直运动的目的即可。Those skilled in the art should understand that the above-mentioned structure of the
如图1和图4所示,在所述凸轮6转动时,所述凸轮6能够沿着推杆3的宽度方向转动,即沿着垂直于图1中纸面方向转动。另外,所述凸轮6也可以沿着推杆3的长度方向转动,即沿着图1中的纸面的左右方向转动,这同样可以实现将推杆3向下推动的目的。As shown in FIGS. 1 and 4 , when the
凸轮6铰接在支撑框架1上以便能够相对于支撑框架1转动,铰接的方式可以是本领域技术人员熟知的各种已知方式。例如,最简单地,通过一根销轴穿过凸轮6和支撑框架1的上侧边即可实现。The
由于支撑框架1的整体厚度可以做的比较薄,例如基本上与方形电池2的厚度相同,或者甚至小于方向电池2的厚度,因此通过销轴直接穿过支撑框架1的上侧边来铰接凸轮6可能会降低支撑框架1的整体强度。因此,如图所示,还可以为凸轮6提供一个凸轮支柱5,该凸轮支柱5上固定有或者一体形成有一个铰轴51,凸轮支柱5则可以通过焊接或者螺纹连接等方式固定在支撑框架1的上侧边11上,然后将凸轮6通过铰轴51可转动地铰接在凸轮支柱5上。由此,即可简单地实现凸轮6与支撑框架1之间的可转动铰接。Since the overall thickness of the
下面对本实用新型的方形电池的焊接夹具的工作过程进行描述。The working process of the welding jig of the square battery of the present invention will be described below.
首先将支撑框架1置于一个平面上,例如工作台平面上,然后将需要焊接到电池外壳上的电池盖板或者电池底盖平行贴紧于支撑框架1的下侧边12的内表面放置,并通过固定于支撑框1的下侧边12内侧的凸台7来定位。然后,将两支方形电池2放入支撑框架1的空间中,使电池外壳紧贴支撑框架1的左右侧边13和14的内侧,并且电池外壳的底边准确定位于电池盖板或电池底盖上。First place the
在将电池2和电池盖板或电池底盖准确放置到支撑框架1中之后,拨动凸轮6,使凸轮6转动。After the battery 2 and the battery cover or the battery bottom cover are accurately placed in the
如图4所示,实线为凸轮6转动之前的状态,此时凸轮面61上的短轴点A和推杆3的上表面接触,此时电池2没有被凸轮6紧固。当凸轮6沿图中的a方向旋转时,将推杆3沿Y轴方向向下推移。当凸轮面61上的远轴点B和推杆3的上表面接触时,如图4中的虚线所示,达到了偏心轮的最大距离和推杆3的最大下行距离,此时也达到了凸轮6的凸轮面61与推杆3的上表面之间的最大摩擦,从而凸轮6可以牢牢地锁死推杆3,而推杆3也可牢牢地紧固电池壳体和盖板或底盖。此时,凸轮6给予推杆3的下压距离X大于电池盖板或底盖的厚度,这样在焊接时就可以使电池壳体和盖板或底盖接触紧密,不致于产生虚焊现象。As shown in FIG. 4 , the solid line is the state before the
然后,将上述装夹好电池2和盖板或底盖的本实用新型的方形电池的焊接夹具整体放置到激光焊机的焊接底座平台上,用气缸等固定装置固定后便可以开始焊接操作,对电池2的外壳和盖板或者外壳和底盖进行焊接。Then, place the welding jig of the square battery of the utility model with the battery 2 and the cover plate or the bottom cover clamped as a whole on the welding base platform of the laser welding machine, and start the welding operation after fixing with a fixing device such as a cylinder. Weld the shell and cover plate or shell and bottom cover of the battery 2 .
在本实用新型中,因凸轮6是按照偏心轮的原理设计,所以只要轻轻拨动凸轮6即可下压推杆3,使电池盖板或底板的左右两边承受均匀的压力,而且,通过对凸轮6的凸轮面61的形状,以及推杆3与支撑框架1的下侧边12之间的距离等进行设计,可以使得在推杆3的下行距离达到最大程度并且凸轮6锁死时,能充分保证电池外壳和盖板或底盖之间的紧密接触。同时,由于在支撑框架1的下侧边12的内侧的中间部分具有凸台7,可以对电池盖板或底盖进行很好的定位。在实施焊接过程中,就可有效防止电池外壳和盖板或底盖的错位,避免电池出现脱焊以及漏液等问题,提高了电池的密封性能以及焊接强度。In the utility model, because the
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2006201664621U CN201002181Y (en) | 2006-12-26 | 2006-12-26 | Welding jig for prismatic batteries |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2006201664621U CN201002181Y (en) | 2006-12-26 | 2006-12-26 | Welding jig for prismatic batteries |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN201002181Y true CN201002181Y (en) | 2008-01-09 |
Family
ID=39037724
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CNU2006201664621U Expired - Fee Related CN201002181Y (en) | 2006-12-26 | 2006-12-26 | Welding jig for prismatic batteries |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN201002181Y (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101618493B (en) * | 2009-07-24 | 2011-11-16 | 苏州宝馨科技实业股份有限公司 | Method for assembling pedestal body of overhead cell support of hybrid vehicle and clamp thereof |
| CN101618490B (en) * | 2009-07-24 | 2011-12-21 | 苏州宝馨科技实业股份有限公司 | Method for assembling overhead cell support of hybrid vehicle and clamp thereof |
| CN107414296A (en) * | 2017-08-18 | 2017-12-01 | 徐平 | A kind of scanning laser welding jigs and fixtures of dynamic battery box high-efficiency and precision manufacture |
| CN113134701A (en) * | 2021-04-29 | 2021-07-20 | 深圳市雄韬电源科技股份有限公司 | Square lithium cell welding frock clamp |
-
2006
- 2006-12-26 CN CNU2006201664621U patent/CN201002181Y/en not_active Expired - Fee Related
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101618493B (en) * | 2009-07-24 | 2011-11-16 | 苏州宝馨科技实业股份有限公司 | Method for assembling pedestal body of overhead cell support of hybrid vehicle and clamp thereof |
| CN101618490B (en) * | 2009-07-24 | 2011-12-21 | 苏州宝馨科技实业股份有限公司 | Method for assembling overhead cell support of hybrid vehicle and clamp thereof |
| CN107414296A (en) * | 2017-08-18 | 2017-12-01 | 徐平 | A kind of scanning laser welding jigs and fixtures of dynamic battery box high-efficiency and precision manufacture |
| CN113134701A (en) * | 2021-04-29 | 2021-07-20 | 深圳市雄韬电源科技股份有限公司 | Square lithium cell welding frock clamp |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102000919A (en) | Laser welding fixture for power batteries | |
| CN116852006A (en) | A kind of docking and fixing equipment for welding and processing of energy storage batteries | |
| CN207205685U (en) | An adjustable lithium battery cover welding fixture | |
| CN203025300U (en) | Clamp suitable for testing lithium ion batteries and cells | |
| CN219224889U (en) | A battery test fixture | |
| CN211103583U (en) | Clamping device for lithium battery machining | |
| CN205985253U (en) | A kind of dismantling device of lithium battery case | |
| CN202127056U (en) | Fixture locating mechanism for laser welding of lug leading sheets and pole | |
| CN2928356Y (en) | A cylindrical battery laser vertical welding fixture | |
| CN203918242U (en) | A kind of welding cap cap device of lithium ion cylinder battery battery core | |
| CN209578475U (en) | A kind of side's housing battery side plate laser welding apparatus | |
| CN206296485U (en) | Detect the drilling equipment of circular lithium ion battery | |
| KR101543063B1 (en) | Jig for welding column type battery cell | |
| CN218692499U (en) | Battery disassembling device | |
| CN214322165U (en) | Soft packet of lithium cell ultrasonic welding anchor clamps | |
| CN209389155U (en) | A kind of battery clamp device | |
| CN215145501U (en) | Spot welding tool of lithium cell package | |
| JP7152071B2 (en) | Battery measuring device using X-ray | |
| WO2024098622A9 (en) | Rolling apparatus and measuring device | |
| CN211062788U (en) | Formation clamp and formation clamp cabinet | |
| CN102593526B (en) | A device for assembling a battery pole group to a battery case | |
| CN211804381U (en) | Ultrasonic welding welding positioning tool for battery cover and all-tab battery pole group | |
| CN220515873U (en) | Auxiliary clamping device for cylindrical cell welding | |
| CN219925045U (en) | A pre-spot welding positioning device for lithium batteries | |
| CN2933686Y (en) | Battery laser welding clamp |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20080109 Termination date: 20151226 |
|
| EXPY | Termination of patent right or utility model |