CN1760006A - Regeneration pelletizer for worn-out plastic - Google Patents
Regeneration pelletizer for worn-out plastic Download PDFInfo
- Publication number
- CN1760006A CN1760006A CNA200510011084XA CN200510011084A CN1760006A CN 1760006 A CN1760006 A CN 1760006A CN A200510011084X A CNA200510011084X A CN A200510011084XA CN 200510011084 A CN200510011084 A CN 200510011084A CN 1760006 A CN1760006 A CN 1760006A
- Authority
- CN
- China
- Prior art keywords
- section
- worn
- out plastic
- piston
- plastic according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B17/00—Recovery of plastics or other constituents of waste material containing plastics
- B29B17/0026—Recovery of plastics or other constituents of waste material containing plastics by agglomeration or compacting
- B29B17/0036—Recovery of plastics or other constituents of waste material containing plastics by agglomeration or compacting of large particles, e.g. beads, granules, pellets, flakes, slices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/50—Details of extruders
- B29C48/505—Screws
- B29C48/53—Screws having a varying channel depth, e.g. varying the diameter of the longitudinal screw trunk
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/50—Details of extruders
- B29C48/505—Screws
- B29C48/565—Screws having projections other than the thread, e.g. pins
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/50—Details of extruders
- B29C48/505—Screws
- B29C48/575—Screws provided with elements of a generally circular cross-section for shearing the melt, i.e. shear-ring elements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/50—Details of extruders
- B29C48/505—Screws
- B29C48/63—Screws having sections without mixing elements or threads, i.e. having cylinder shaped sections
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02W—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO WASTEWATER TREATMENT OR WASTE MANAGEMENT
- Y02W30/00—Technologies for solid waste management
- Y02W30/50—Reuse, recycling or recovery technologies
- Y02W30/62—Plastics recycling; Rubber recycling
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Environmental & Geological Engineering (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
Abstract
Description
技术领域technical field
本发明涉及将废旧塑料回收再生制造塑料颗粒的设备技术领域。The invention relates to the technical field of equipment for recycling waste plastics to produce plastic granules.
背景技术Background technique
目前,市场上销售的废旧塑料再生造粒机多数为普通造粒机。其结构主要采用一般的挤出机+普通过滤器+模头+冷却装置+破碎装置的结构;或者挤出机+普通过滤器+模头+热切风冷的结构。这两种结构的普通过滤器的过滤面较小,也不能自动检测料压,不能准确判断是否需更换滤网,过滤杂质效果不佳,再造的塑料粒子的质量难以控制。此外,上述第一种结构的造粒机,塑料通过模头拉成条状进入冷却装置,是在冷却后破碎成粒子,粒子的切割面不光滑规整,粒子长度也不易控制;第二种结构的造粒机,塑料是用空气冷却,切碎的粒子会随高速气流在风管里飞行,杂乱无章地撞在管壁上,将尚未完全冷却的塑料粒子撞成各种大小不一的扁平状粒子。两种结构的造粒机再造的塑料粒子粒度、形状均不均匀,质量较差,影响后续生产应用。而且由于所采用的均为不排气式的挤出机,故不能加工湿料。At present, most of the waste plastic recycling granulators sold on the market are ordinary granulators. Its structure mainly adopts the structure of general extruder + ordinary filter + die head + cooling device + crushing device; or the structure of extruder + ordinary filter + die head + eager air cooling. The filter surface of the ordinary filter of these two structures is small, and the material pressure cannot be automatically detected, and it is impossible to accurately judge whether to replace the filter screen, the effect of filtering impurities is not good, and the quality of the regenerated plastic particles is difficult to control. In addition, in the granulator of the above-mentioned first structure, the plastic is drawn into strips through the die head and enters the cooling device, and is broken into particles after cooling. The cutting surface of the particles is not smooth and regular, and the length of the particles is not easy to control; the second structure The plastic is cooled by air, and the chopped particles will fly in the air duct with the high-speed airflow, hit the wall of the tube in a disorderly manner, and smash the plastic particles that have not been completely cooled into flat shapes of various sizes. particle. The plastic particles remanufactured by the two structures of the granulator are uneven in particle size and shape, and the quality is poor, which affects subsequent production and application. And because all the extruders used are non-vented extruders, wet materials cannot be processed.
发明内容Contents of the invention
本发明的目的正是为了解决上述现有技术存在的不足而提供一种能够生产出粒度均匀、外型光滑的高质量的成型粒子,并可回收多类废旧塑料以及湿料的废旧塑料再生造粒机。The purpose of the present invention is to solve the above-mentioned deficiencies in the prior art and to provide a waste plastic recycling system that can produce high-quality shaped particles with uniform particle size and smooth appearance, and can recycle many types of waste plastics and wet materials. Granulator.
本发明的目的是通过如下技术方案实现的。The purpose of the present invention is achieved through the following technical solutions.
废旧塑料再生造粒机,包括顺序连接的排气式挤出机和切割造粒机。Waste plastic recycling granulator, including sequentially connected exhaust type extruder and cutting granulator.
本发明在排气式挤出机和切割造粒机之间还设置有过滤器;在切割造粒机后面还连接有螺旋输送机、干燥机和风送系统;所述的排气式挤出机包括带排气孔的机筒和设置于机筒内的排气式螺杆,所述的排气式螺杆包括第一阶螺杆和第二阶螺杆,第一阶螺杆包括加料段、变径压缩段、计量段和混炼段,还包括紧接混炼段的调压段;第二阶螺杆包括排气段、突变段,以及紧接的计量段;排气式螺杆的长度与外径的比值为35~45;第二阶螺杆与第一阶螺杆的长度比为0.5~0.8;混炼段由两段组成,第一段是螺纹间断的断续状螺纹段,第二段是在底杆上设置销钉状的环槽;第二阶螺杆计量段的长度与外径的比值为6~13;在挤出机机筒上对应调压段的位置,设置有调压阀;所述的过滤器包括料液通道体和对称连接于通道体两侧的上活塞体和下活塞体;通道体中横向设置有相对的两个“Y”型或“T”型料液通道,一个通道分别通向料液进口和上下活塞,另一个通道分别通向料液出口和上下活塞;截面为束腰形的活塞设置于活塞体的柱形空腔内将活塞腔分隔为左、右腔体,设置在活塞上的喷嘴将左右腔体连通,活塞与液压杆连接,在左、右活塞腔体内对称顺序装有过滤板、滤网和支撑板,在活塞和活塞体上开设有将左、右活塞腔与通向料液出口的“Y”型或“T”型料液通道连通的通路;在活塞体上开设有分别将左、右活塞腔中料液渣引出的引渣道;在通道体、上活塞体和下活塞体上设置有加热装置;所述的切割造粒机包括有模头、设置于模头外面的水仓体和与水仓体连接的筒体,在水仓体与筒体之间设置有喷嘴,在筒体内设置有转轴,转轴的前端安装有用于安装切刀的刀座,切刀对向模头上的出料孔,转轴的后端通过联接套与电机联结;在筒体上设置有观察窗;水仓体与筒体之间的连接方式是,一侧通过铰链连接,另一侧通过搭扣连接;在联接套上设置有调刀装置,调刀装置的悬臂穿过联结套与转轴的外套联结。In the present invention, a filter is also arranged between the exhaust extruder and the cutting granulator; behind the cutting granulator, a screw conveyor, a dryer and an air delivery system are also connected; the exhaust extruder It includes a barrel with a vent hole and a venting screw arranged in the barrel. The venting screw includes a first-stage screw and a second-stage screw. The first-stage screw includes a feeding section and a variable-diameter compression section. , the metering section and the mixing section, including the pressure regulating section immediately after the mixing section; the second-stage screw includes the exhaust section, the sudden change section, and the next metering section; the ratio of the length of the exhaust screw to the outer diameter The length ratio of the second-stage screw to the first-stage screw is 0.5-0.8; the mixing section consists of two sections, the first section is an intermittent thread section with intermittent threads, and the second section is at the bottom rod A pin-shaped ring groove is set on the top; the ratio of the length of the second-stage screw metering section to the outer diameter is 6 to 13; a pressure regulating valve is provided on the barrel of the extruder corresponding to the pressure regulating section; the filtering The device consists of a material-liquid channel body and an upper piston body and a lower piston body symmetrically connected to both sides of the channel body; two opposite "Y" or "T"-shaped material-liquid channels are arranged laterally in the channel body, and one channel is respectively connected to the To the feed liquid inlet and the upper and lower pistons, the other channel leads to the feed liquid outlet and the upper and lower pistons respectively; the waist-shaped piston with cross-section is set in the cylindrical cavity of the piston body to divide the piston cavity into left and right cavities. The nozzle on the piston connects the left and right chambers, and the piston is connected with the hydraulic rod. Filter plates, filter screens and support plates are installed in a symmetrical order in the left and right piston chambers. The cavity communicates with the "Y" type or "T" type material liquid channel leading to the material liquid outlet; on the piston body, there are slag guide channels to lead out the material liquid slag in the left and right piston chambers respectively; on the channel body , The upper piston body and the lower piston body are provided with a heating device; the cutting granulator includes a die head, a water bin body arranged outside the die head and a cylindrical body connected with the water bin body, between the water bin body and the water bin body Nozzles are arranged between the barrels, and a rotating shaft is arranged in the barrel. A knife seat for installing a cutter is installed on the front end of the rotating shaft. The cutter faces the discharge hole on the die head, and the rear end of the rotating shaft is connected to the motor through a coupling sleeve. ; There is an observation window on the cylinder; the connection between the tank body and the cylinder is that one side is connected by a hinge, and the other side is connected by a buckle; The cantilever passes through the coupling sleeve and is connected with the outer cover of the rotating shaft.
本发明结构合理,极大的提高了设备生产的连续性,可大大提高塑料粒子的产量。The invention has a reasonable structure, greatly improves the continuity of equipment production, and can greatly increase the output of plastic particles.
所采用的排气式挤出机的结构,使废旧塑料通过加料段、压缩段、计量段和混炼段时,在压缩段下被逐渐熔化,在计量段被混合和剪切,在混炼段被进一步塑化后进入调压段,在调压段通过调节塑料流通的面积,可调节进入排气段的塑料,防止塑料从机筒的排气口冒出。塑料进入排气段通过设置在机筒上的排气口排出水气和分解物后,在突变段再一次被压实,在计量段进一步混合、剪切后,通过计量段,定量、定压挤入后续设备中。由于螺杆长径比较大,在高速转动下,塑料在螺杆中的停留时间加长,有利于塑料的塑化。所采用的混炼段的结构,使螺杆在高速转动下,可以将未熔化的塑料,进一步地混合与剪切,进行塑化。第二阶螺杆与第一阶螺杆的长度比设计,使塑料的塑化和排气效果均能得到有效的提高。第二阶螺杆计量段的长径比设计,使得较长的第二阶螺杆计量段即使在前端压力过高时,料流的逆流也很小。从而减小冒料口冒料的可能性,并能使产量提高。所设置的调压段可调节对应在机筒上安装的调压阀,控制第一阶螺杆塑料的挤出量,使之与第二阶螺杆的挤出量匹配,进一步减小了冒料口冒料的可能性。该挤出机在高速下工作,塑化质量较高,产量高,适用面广,可用于PE、PP、PET、PS、PC等各种废旧塑料干料和湿料的回收处理。The structure of the exhaust extruder is adopted, so that when the waste plastic passes through the feeding section, compression section, metering section and mixing section, it is gradually melted under the compression section, mixed and sheared in the metering section, and mixed and sheared in the mixing section. After being further plasticized, the plastic section enters the pressure regulating section. In the pressure regulating section, by adjusting the plastic circulation area, the plastic entering the exhaust section can be adjusted to prevent the plastic from emerging from the exhaust port of the barrel. After the plastic enters the exhaust section and discharges water vapor and decomposition products through the exhaust port on the barrel, it is compacted again in the sudden change section, and after further mixing and shearing in the metering section, it passes through the metering section, quantitative and constant pressure Squeeze into subsequent equipment. Due to the relatively large length and diameter of the screw, the residence time of the plastic in the screw is prolonged under high-speed rotation, which is beneficial to the plasticization of the plastic. The structure of the mixing section adopted enables the screw to further mix and shear the unmelted plastic under high-speed rotation for plasticization. The length ratio design of the second-stage screw and the first-stage screw can effectively improve the plasticizing and exhausting effects of the plastic. The length-to-diameter ratio design of the second-stage screw metering section makes the reverse flow of the material flow very small even when the front-end pressure of the longer second-stage screw metering section is too high. Thereby reducing the possibility of material leakage from the feeder mouth and increasing the output. The set pressure regulating section can be adjusted to correspond to the pressure regulating valve installed on the barrel to control the extrusion volume of the first-stage screw plastic to match the extrusion volume of the second-stage screw, further reducing the discharge port. Possibility of cheating. The extruder works at high speed, has high plasticizing quality, high output, and wide application range. It can be used for recycling and processing various waste plastic dry and wet materials such as PE, PP, PET, PS, and PC.
所采用的过滤器的结构,可通过所设置的控制系统监测滤网受到的压力,并及时启动液压系统工作,通过处于工作状态的滤网流出的干净熔液,从背面流入对面的过滤网对其进行反冲洗,将滞留在滤网正面的料液渣冲出机体。在一个滤网进行反冲清洗时,其余三个滤网仍处于过滤状态,因此,在清洗过程中,滤网受到的料液压力增高极小。防止因压力过高影响挤出机产量,避免过滤后的料液含杂质量过高。由于滤网得到冲洗,清洁程度得以显著提高,可以大大延长滤网使用寿命,减少更换滤网。既使是需要更换一个活塞体中的滤网时,另一个活塞体仍然可以正常工作,完全实现不停机换网。本实用新型的结构还使得在正常工作条件下,料液的过滤面扩大一倍,对称设置的滤网支承板使得料液可以从两侧对滤网施加相同的压力,均衡施加在活塞上的压力,从而减少活塞和滤网的磨损。所设置的加热装置使通道体和活塞体保持一定温度以防止流过的料液温度降低而减低流动性。The structure of the filter used can monitor the pressure on the filter screen through the set control system, and start the hydraulic system to work in time. The clean melt flowing out of the filter screen in the working state flows into the opposite filter screen from the back. It performs backwashing to flush out the liquid residue remaining on the front of the filter screen out of the body. When one filter screen is backwashed, the other three screens are still in the filtering state. Therefore, during the cleaning process, the increase in the pressure of the feed liquid on the filter screen is minimal. Prevent the output of the extruder from being affected by too high pressure, and prevent the impurity content of the filtered feed liquid from being too high. Since the filter screen is flushed, the cleaning degree can be significantly improved, which can greatly extend the service life of the filter screen and reduce the replacement of the filter screen. Even when the filter screen in one piston body needs to be replaced, the other piston body can still work normally, completely realizing non-stop screen replacement. The structure of the utility model also makes the filter surface of the feed liquid doubled under normal working conditions, and the symmetrically arranged filter screen support plate enables the feed liquid to exert the same pressure on the filter screen from both sides, and evenly applies the pressure on the piston. pressure, thereby reducing wear on pistons and screens. The provided heating device keeps the channel body and the piston body at a certain temperature so as to prevent the fluidity from being lowered due to the temperature drop of the material liquid flowing through.
所采用的切割造粒机将熔融的塑料通过的模头上的出料孔分流成多股料流。当塑料从出料孔挤出时,高速旋转的切刀把塑料切割成细小颗粒。并在离心力的作用下,塑料粒子被抛甩到圆筒上的水环内冷却和凝固。随着水环的流动,固化的塑料粒子随水流出筒体。所设置的观察窗,可在调节切刀的过程中清楚地看见切刀的压紧情况,并检查每把切刀是否均匀地压在模头上。同时,可以清楚地看见筒壁的水环是否形成,避免水流到模头上,降低模头温度,造成模头被凝固的塑料堵死的事故。所采用的水仓体与筒体之间的联接结构,使模头与筒体部分易于打开,便于快速更换切刀,减少停机时间。所设置的调刀装置,可调节切刀与模头的距离,使切刀以较小的压力压在模头上,减小模头和切刀的磨损,也使切刀的变形最小,延长使用寿命。该造粒机再造的塑料粒子颗粒均匀,外型光滑规整,质量好。The cutting granulator used divides the molten plastic through the discharge hole on the die head into multiple streams. When the plastic is extruded from the discharge hole, the high-speed rotating cutter cuts the plastic into fine particles. And under the action of centrifugal force, the plastic particles are thrown into the water ring on the cylinder to cool and solidify. With the flow of the water ring, the solidified plastic particles flow out of the cylinder with the water. The set observation window can clearly see the pressing condition of the cutting knife during the adjustment of the cutting knife, and check whether each cutting knife is evenly pressed on the die head. At the same time, you can clearly see whether the water ring on the wall of the cylinder is formed, so as to prevent the water from flowing onto the die, reducing the temperature of the die, and causing the die to be blocked by solidified plastic. The connection structure between the water tank body and the cylinder body adopted makes it easy to open the die head and the cylinder body, which facilitates quick replacement of the cutter and reduces downtime. The set knife adjustment device can adjust the distance between the cutter and the die head, so that the cutter is pressed on the die head with a small pressure, which reduces the wear of the die head and the cutter, and also minimizes the deformation of the cutter and prolongs the life of the cutter. service life. The plastic particles regenerated by this granulator are uniform in size, smooth in appearance and good in quality.
下面结合说明书附图进一步阐述本发明的内容。The content of the present invention will be further elaborated below in conjunction with the accompanying drawings.
附图说明Description of drawings
图1是本发明的主视图;Fig. 1 is the front view of the present invention;
图2是本发明的俯视图;Fig. 2 is a top view of the present invention;
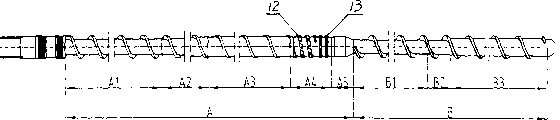
图3是排气式挤出机的排气螺杆的结构示意图;Fig. 3 is the structural representation of the exhaust screw of exhaust type extruder;
图4是排气式挤出机在调压段螺杆与机筒和调压阀配合的截面示意图;Fig. 4 is a schematic cross-sectional view of the cooperation of the screw, the barrel and the pressure regulating valve in the pressure regulating section of the vented extruder;
图5是过滤器的结构示意图;Fig. 5 is the structural representation of filter;
图6是图5的A-A剖视图;Fig. 6 is A-A sectional view of Fig. 5;
图7是图5的右视图;Fig. 7 is the right view of Fig. 5;
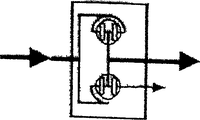
图8是过滤器活塞正常工作状态的示意图;Fig. 8 is a schematic diagram of the normal working state of the filter piston;
图9是过滤器下活塞体右滤网处于反冲洗状态的示意图;Fig. 9 is a schematic diagram of the right filter screen of the lower piston body of the filter in a backwashing state;
图10是过滤器下活塞体左滤网处于反冲洗状态的示意图;Fig. 10 is a schematic diagram of the left filter screen of the lower piston body of the filter in a backwashing state;
图11是切割造粒机的主视剖视图;Figure 11 is a front sectional view of the cutting granulator;
图12是图10的俯视图。FIG. 12 is a top view of FIG. 10 .
具体实施方式Detailed ways
如图1、图2所示,本发明由顺序连接的排气式挤出机1、过滤器2、切割造粒机3、螺旋输送机4、干燥机5和风送系统6组成。As shown in Fig. 1 and Fig. 2, the present invention consists of a vented extruder 1, a filter 2, a cutting granulator 3, a screw conveyor 4, a
如图3所示,排气式挤出机1包括第一阶螺杆A和第二阶螺杆B,第一阶螺杆A包括加料段A1、压缩段A2、计量段A3和混炼段A4,还包括紧接混炼段的调压段A5;第二阶螺杆B包括排气段B1、突变段B2,以及紧接的计量段B3。螺杆的长度与外径的比值为35~45,本实施例选择40;第二阶螺杆B与第一阶螺杆A的长度比为0.5~0.8,本实施例选择0.7;混炼段A4由两段组成,第一段是螺纹12间断的断续状螺纹段,第二段是在底杆上设置销钉状的环槽13;第二阶螺杆计量段B3的长度与外径的比值为6~13,本实施例选择10;如图4所示,在挤出机机筒14上对应调压段A5的位置,设置有调压阀15。As shown in Figure 3, the exhaust extruder 1 comprises a first-stage screw A and a second-stage screw B, and the first-stage screw A comprises a feeding section A1, a compression section A2, a metering section A3 and a mixing section A4, and Including the pressure regulating section A5 next to the mixing section; the second-stage screw B includes the exhaust section B1, the sudden change section B2, and the next metering section B3. The ratio of the length to the outer diameter of the screw is 35-45, and 40 is selected in this embodiment; the length ratio of the second-stage screw B to the first-stage screw A is 0.5-0.8, and 0.7 is selected in this embodiment; the mixing section A4 is composed of two The first section is a discontinuous thread section with
如图5、图6、图7所示,过滤器2包括料液通道体16和对称连接于通道体两侧的上活塞体17和下活塞体18;通道体中横向设置有相对的两个“Y”型或“T”型料液通道19和20,本实施例为“Y”型通道,通道19分别通向料液进口和上、下活塞,通道20分别通向料液出口和上、下活塞;截面为束腰形的活塞21设置于活塞体的柱形空腔内将活塞腔分隔为左、右腔体,设置在活塞上的喷嘴22将左、右腔体连通,活塞与液压杆23连接,液压系统可推动活塞在活塞腔内前后移动。在左、右活塞腔体内对称顺序装有过滤板24、滤网25和支撑板26,滤网25由3~5层滤网构成。在活塞和活塞体上开设有将左、右活塞腔与通向料液出口的“Y”型通道20连通的通路27、27′;在活塞体上开设有分别将左、右活塞腔中料液渣引出的引渣道28、28′;在通道体16、上活塞体17和下活塞体18上设置有加热装置29。As shown in Fig. 5, Fig. 6 and Fig. 7, the filter 2 includes a feed liquid channel body 16 and an upper piston body 17 and a lower piston body 18 symmetrically connected to both sides of the channel body; "Y" or "T" type feed liquid channels 19 and 20, this embodiment is a "Y" type channel, channel 19 leads to feed liquid inlet and upper and lower piston respectively, channel 20 leads to feed liquid outlet and upper piston respectively , lower piston; the cross-section is that the waist-shaped piston 21 is arranged in the cylindrical cavity of the piston body and the piston chamber is divided into left and right chambers, and the nozzle 22 arranged on the piston communicates with the left and right chambers, and the piston and the right chamber are connected. The
如图10、图11所示,切割造粒机3包括有模头30、设置于模头外面的水仓体31和与水仓体连接的筒体33,模头30和水仓体31用螺栓连接在一起,固定不动,在水仓体与筒体之间设置有喷嘴34,水仓体31与筒体33之间的连接方式是,一侧通过铰链42连接,另一侧通过搭扣43连接。在筒体内设置有转轴35,转轴35的前端安装有用于安装切刀36的刀座37,切刀对向模头上的出料孔38,转轴的后端通过联接套39与电机40联结。在筒体上设置有观察窗41。在联接套39上设置有调刀装置44,调刀装置的悬臂45穿过联结套与转轴35的外套46联结。As shown in Figure 10 and Figure 11, the cutting granulator 3 includes a die head 30, a water tank body 31 arranged outside the die head and a
工作过程如下:废旧塑料颗粒通过挤出机的进料口进入机筒内第一阶螺杆A的加料段A1,螺杆在转动下把塑料往前推动,在往前推动过程中,塑料被压实进入压缩段A2,塑料在压缩下被逐渐熔化。熔化后的塑料被挤入计量段A3。计量段A3主要使塑料混和和剪切。并以一定的量挤入混炼段A4,进一步使未熔化的塑料塑化。通过调压段A5时,通过设置在机筒上的调压阀2可调节塑料流通面积,从而调节进入第二阶螺杆B的排气段B 1的塑料流量,防止进入排气段的塑料从机筒上的排气口冒出。塑料在排气段B1排出水气和分解物后。在突变段B2再一次被压实,在计量段进一步混合、剪切后,通过计量段B3,定量、定压挤入过滤器2中,如图8、图6所示,在正常工作状态。料液沿图8中箭头方向流过,经图6中活塞21两侧对称设置的支撑板26、滤网25、过滤板24、进入活塞内部再经通路27、27′由出口通道20流出。当下活塞体18中的活塞右侧过滤网处的料液压力达到设定值时,设置在进料通道19前端挤出机上的传感器检测到压力信号传输到控制系统,控制系统启动液压系统,进入反冲洗状态,如图9所示,料液将从下活塞的左侧通道经过滤网进入,右侧不再进料,在压力作用下,料液流经喷嘴22出口时将呈喷射状,并以极快的速度冲洗右侧的过滤板和滤网,从而达到反冲洗的目的,被冲洗下来的料液渣沿引渣道28被排出机体。图10所示的反冲洗过程则正好与图9相反。上活塞的反冲洗也是同样道理。由于反冲洗后滤网处的压力始终比反冲洗前要高,因此,当反冲洗一定次数之后,反冲洗处在刚冲洗完时的压力接近设定值时,即需更换过滤网。从过滤器流出的料液接着流入切割造粒机3。预先调整好切割造粒机的工作状态,旋转调刀装置横向螺杆47上的调节螺套48,通过悬臂45和套在转轴35上的外套46推动转轴前行,使切刀36靠贴于模头30的端面。将冷却水从进水口49注入水仓50,由喷嘴34喷向筒体内壁形成水环。熔融的塑料从模头的进料通道51进入,通过模头30上沿圆周均布的多个出料孔38分流成多股料流。当塑料从出料孔道中挤出来的时候,由电机40带动高速旋转的切刀36把塑料切割成细小颗粒。在离心力的作用下,塑料粒子被抛甩到筒体33上的水环52内被冷却和凝固。随着水环的流动,固化的塑料粒子随水流出筒体33。当需要换刀或清理时,松开搭扣43,沿铰链42转动筒体33,打开造粒头,及时换刀或清理。至此,完成废旧塑料在造粒头中的粒子成型的全过程。之后,螺旋输送机36把大部分水排出后,剩下的成形粒子被送入离心干燥机37内。在高速离心力的作用下成形粒子被彻底的甩干。同时,由离心干燥机的出料口11进入风送系统6,并通过风的作用,把成形粒子吹进落料器中。至此,完成了整个废旧塑料的再造和回收过程。The working process is as follows: waste plastic particles enter the feeding section A1 of the first stage screw A in the barrel through the feed port of the extruder, and the screw pushes the plastic forward under the rotation, and the plastic is compacted during the forward pushing process Entering the compression section A2, the plastic is gradually melted under compression. The melted plastic is extruded into metering section A3. The metering section A3 mainly mixes and shears the plastic. And squeeze into the mixing section A4 with a certain amount to further plasticize the unmelted plastic. When passing through the pressure regulating section A5, the plastic flow area can be adjusted through the pressure regulating valve 2 arranged on the barrel, thereby adjusting the plastic flow rate entering the exhaust section B1 of the second-stage screw B, preventing the plastic entering the exhaust section from flowing The exhaust port on the barrel pops out. After the plastic discharges water vapor and decomposition products in the exhaust section B1. It is compacted again in the sudden change section B2, and after further mixing and shearing in the metering section, it passes through the metering section B3 and squeezes into the filter 2 quantitatively and at a constant pressure, as shown in Fig. 8 and Fig. 6 , in normal working condition. The feed liquid flows along the direction of the arrow in Fig. 8, and enters the interior of the piston through the support plate 26, filter screen 25, and filter plate 24 arranged symmetrically on both sides of the piston 21 in Fig. 6, and then flows out from the outlet channel 20 through passages 27, 27'. When the feed liquid pressure at the filter screen on the right side of the piston in the lower piston body 18 reaches the set value, the sensor arranged on the extruder at the front end of the feed channel 19 detects the pressure signal and transmits it to the control system, and the control system starts the hydraulic system and enters In the backwash state, as shown in Figure 9, the feed liquid will enter from the left channel of the lower piston through the filter screen, and the right side will no longer feed. Under the action of pressure, the feed liquid will be sprayed when it flows through the outlet of the nozzle 22. And flush the filter plate and filter screen on the right side at an extremely fast speed, so as to achieve the purpose of backwashing, and the washed material liquid slag is discharged from the body along the
本发明既能有效开发利用废旧塑料资源,又可治理污染,同时创造巨大的经济和环境效益,是利国利民的绿色环保设备。The invention can not only effectively develop and utilize waste plastic resources, but also control pollution, and simultaneously create huge economic and environmental benefits, and is a green environmental protection equipment that benefits the country and the people.
Claims (14)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNB200510011084XA CN100540251C (en) | 2005-10-26 | 2005-10-26 | Regeneration pelletizer for worn-out plastic |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNB200510011084XA CN100540251C (en) | 2005-10-26 | 2005-10-26 | Regeneration pelletizer for worn-out plastic |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN1760006A true CN1760006A (en) | 2006-04-19 |
| CN100540251C CN100540251C (en) | 2009-09-16 |
Family
ID=36706282
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CNB200510011084XA Expired - Fee Related CN100540251C (en) | 2005-10-26 | 2005-10-26 | Regeneration pelletizer for worn-out plastic |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN100540251C (en) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101204837B (en) * | 2007-10-12 | 2010-05-19 | 东莞市蓝冠机械设备有限公司 | Recycling and granulation process of waste high foaming plastic |
| CN101941253A (en) * | 2010-08-16 | 2011-01-12 | 无锡创达电子有限公司 | Thermo-setting plastic pelleting method and device |
| CN102147188A (en) * | 2011-04-25 | 2011-08-10 | 张家港白熊科美机械有限公司 | Film extruding machine |
| CN102785299A (en) * | 2012-08-21 | 2012-11-21 | 六安市洁美再生物资回收有限公司 | Polystyrene foam recovery granulating process |
| CN103286878A (en) * | 2013-06-19 | 2013-09-11 | 汕头市富达塑料机械有限公司 | Plastic extrusion granulating unit |
| CN103934918A (en) * | 2014-04-24 | 2014-07-23 | 江苏方圣机械有限公司 | Granulating production line for recycling waste plastics |
| CN103358529B (en) * | 2012-04-09 | 2016-01-20 | 青岛福润德塑料挤出技术有限公司 | Three-stage type efficiently plastifies filtering exhaust plastic extrusion system |
| CN106945193A (en) * | 2017-05-19 | 2017-07-14 | 唐山鼎业塑材科技有限公司 | A kind of waste or used plastics Single screw extrusion Granulation Equipments and technique |
| CN108928649A (en) * | 2018-09-07 | 2018-12-04 | 曾金玉 | A kind of granulation charging gear |
| CN109203414A (en) * | 2018-09-30 | 2019-01-15 | 马鞍山沐及信息科技有限公司 | A kind of extrusion mechanism in pelletizer |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2065975U (en) * | 1989-09-23 | 1990-11-21 | 大连景山通风设备厂 | Polypropylene plastics waste film reclaimed prill machine group |
| CN2194253Y (en) * | 1994-03-22 | 1995-04-12 | 北京化工学院 | Wet Waste Plastic Film Pelletizing Extruder |
| CN2740378Y (en) * | 2004-09-20 | 2005-11-16 | 南京工业职业技术学院 | Polyester plastic recovering device with single screw |
| CN2841302Y (en) * | 2005-10-26 | 2006-11-29 | 云南昆船设计研究院 | Waste-plastic regeneration granule-making machine |
-
2005
- 2005-10-26 CN CNB200510011084XA patent/CN100540251C/en not_active Expired - Fee Related
Cited By (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101204837B (en) * | 2007-10-12 | 2010-05-19 | 东莞市蓝冠机械设备有限公司 | Recycling and granulation process of waste high foaming plastic |
| CN101941253A (en) * | 2010-08-16 | 2011-01-12 | 无锡创达电子有限公司 | Thermo-setting plastic pelleting method and device |
| CN102147188A (en) * | 2011-04-25 | 2011-08-10 | 张家港白熊科美机械有限公司 | Film extruding machine |
| CN103358529B (en) * | 2012-04-09 | 2016-01-20 | 青岛福润德塑料挤出技术有限公司 | Three-stage type efficiently plastifies filtering exhaust plastic extrusion system |
| CN102785299A (en) * | 2012-08-21 | 2012-11-21 | 六安市洁美再生物资回收有限公司 | Polystyrene foam recovery granulating process |
| CN103286878A (en) * | 2013-06-19 | 2013-09-11 | 汕头市富达塑料机械有限公司 | Plastic extrusion granulating unit |
| CN103286878B (en) * | 2013-06-19 | 2015-10-28 | 汕头市富达塑料机械有限公司 | Plastic extruding pelletization unit |
| CN103934918A (en) * | 2014-04-24 | 2014-07-23 | 江苏方圣机械有限公司 | Granulating production line for recycling waste plastics |
| CN106945193A (en) * | 2017-05-19 | 2017-07-14 | 唐山鼎业塑材科技有限公司 | A kind of waste or used plastics Single screw extrusion Granulation Equipments and technique |
| CN108928649A (en) * | 2018-09-07 | 2018-12-04 | 曾金玉 | A kind of granulation charging gear |
| CN109203414A (en) * | 2018-09-30 | 2019-01-15 | 马鞍山沐及信息科技有限公司 | A kind of extrusion mechanism in pelletizer |
Also Published As
| Publication number | Publication date |
|---|---|
| CN100540251C (en) | 2009-09-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2116659C (en) | Apparatus for filtering and extruding synthetic plastic scrap material | |
| CN207224519U (en) | A kind of injection moulding apparatus of horizontal injection press | |
| US6328919B1 (en) | Method for extruding polycarbonate of low bulk density | |
| CN205202062U (en) | Conical twin screw extruder | |
| CN100540251C (en) | Regeneration pelletizer for worn-out plastic | |
| CN1096978A (en) | Synthetic Resin Granulator | |
| CN219968766U (en) | Agglomerated plastic particle scattering and recycling device | |
| CN2058879U (en) | Hydraulic two-working-position filting converting device | |
| CN2841302Y (en) | Waste-plastic regeneration granule-making machine | |
| CN212097466U (en) | Intermediate screen changer for extruder | |
| CN103358529B (en) | Three-stage type efficiently plastifies filtering exhaust plastic extrusion system | |
| CN211590883U (en) | Granulation production line | |
| CN112793033A (en) | Stable extrusion granulation device for wood-plastic composites | |
| CN219486243U (en) | Plastic master batch extrusion device | |
| CN222875247U (en) | A conical twin-screw extruder with waste recycling function | |
| CN222610089U (en) | Plastic masterbatch extrusion device | |
| US20240326291A1 (en) | Device and method for processing plastic material | |
| CN222201614U (en) | Extruder head of granulator | |
| CN221456732U (en) | Screw extruder after broken marine plastic broken fishing net | |
| CN222004379U (en) | Parallel double-screw extrusion cabinet | |
| CN211807724U (en) | Extruding machine | |
| CN220534640U (en) | Extrusion molding granulator | |
| CN224158837U (en) | An adjustable, non-removable twin-screw extruder die | |
| CN223223823U (en) | Thermoplastic extrusion equipment | |
| CN214353815U (en) | Injection device of injection molding machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20090916 |