CN116423047A - A sensor automatic laser welding device - Google Patents
A sensor automatic laser welding device Download PDFInfo
- Publication number
- CN116423047A CN116423047A CN202310611761.XA CN202310611761A CN116423047A CN 116423047 A CN116423047 A CN 116423047A CN 202310611761 A CN202310611761 A CN 202310611761A CN 116423047 A CN116423047 A CN 116423047A
- Authority
- CN
- China
- Prior art keywords
- fixed
- welding device
- laser welding
- box
- working box
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/20—Bonding
- B23K26/21—Bonding by welding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/14—Working by laser beam, e.g. welding, cutting or boring using a fluid stream, e.g. a jet of gas, in conjunction with the laser beam; Nozzles therefor
- B23K26/142—Working by laser beam, e.g. welding, cutting or boring using a fluid stream, e.g. a jet of gas, in conjunction with the laser beam; Nozzles therefor for the removal of by-products
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/70—Auxiliary operations or equipment
- B23K26/702—Auxiliary equipment
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/70—Auxiliary operations or equipment
- B23K26/702—Auxiliary equipment
- B23K26/703—Cooling arrangements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K37/00—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass
- B23K37/04—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass for holding or positioning work
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Mechanical Engineering (AREA)
- Plasma & Fusion (AREA)
- Laser Beam Processing (AREA)
Abstract
本发明涉及一种传感器全自动激光焊接装置,包括工作箱,所述工作箱顶面的左右两侧均固定有支撑板,两个所述支撑板的顶面固定有顶板,所述工作箱上设有焊接机构,所述工作箱上设有固定夹持机构,所述工作箱上设有辅助机构,所述辅助机构包括固定台,所述固定台固定在工作箱的正面,所述固定台的顶面固安装有风机,所述风机的输出端固定有出风管,所述出风管的外表固定有固定块。该传感器全自动激光焊接装置,设有辅助机构,通过风机吹出冷风,并由出风管输送至喷风头喷出对工件表面进行降温,可快速将工件取下,同时可通过抽风机的抽风作用,通过抽风罩将焊接过程中的焊渣进行清理,避免焊渣影响工件的焊接质量。
The invention relates to a sensor full-automatic laser welding device, which comprises a work box, support plates are fixed on the left and right sides of the top surface of the work box, and top plates are fixed on the top surfaces of the two support plates. A welding mechanism is provided, the work box is provided with a fixed clamping mechanism, the work box is provided with an auxiliary mechanism, the auxiliary mechanism includes a fixed platform, and the fixed platform is fixed on the front of the work box, and the fixed platform A fan is fixedly installed on the top surface of the fan, an air outlet pipe is fixed at the output end of the fan, and a fixed block is fixed on the outer surface of the air outlet pipe. The sensor automatic laser welding device is equipped with an auxiliary mechanism. The cold air is blown out by the fan and sent to the air nozzle by the air outlet pipe to cool down the surface of the workpiece, and the workpiece can be quickly removed. At the same time, the exhaust fan can be used , Clean up the welding slag during the welding process through the exhaust hood to prevent the welding slag from affecting the welding quality of the workpiece.
Description
技术领域technical field
本发明涉及激光焊接技术领域,具体为一种传感器全自动激光焊接装置。The invention relates to the technical field of laser welding, in particular to a fully automatic laser welding device for sensors.
背景技术Background technique
现代电子产品生产、光通讯、家用电器等很多领域均需要电路板提供控制与信号单元,随着电子元器件的小型化以及大量集成电路的使用,焊点越来越小,焊点之间的间距也越来越小,这样对电路板元器件的焊接提出了越来越高的要求。Modern electronic product production, optical communication, household appliances and many other fields require circuit boards to provide control and signal units. With the miniaturization of electronic components and the use of a large number of integrated circuits, solder joints are getting smaller and smaller, and the distance between solder joints The spacing is also getting smaller and smaller, which puts forward higher and higher requirements for the soldering of circuit board components.
例如中国专利(公共号:CN 103962721 B)中公开了激光焊接头及激光焊接机,包括底板,底板上安装有固定块和储料仓,固定块的侧壁上分别设有进气口和进料通道,固定块的底部安装有出锡嘴,固定块的顶部安装有激光器光纤头,储料仓底部设有出料通孔,地板上设有与进料通道相连通的下落通道,底板上滑动安装有由直线驱动装置驱动的分料滑块,分料滑块上设有定位孔,使用气缸带动分料滑块滑动,从而将锡球推入出锡嘴的出口处,然后利用激光束将锡球融化,锡球在保护气的压力作用下从出锡嘴的出口喷出,从而进行焊接。For example, the Chinese patent (public number: CN 103962721 B) discloses a laser welding head and a laser welding machine, including a base plate on which a fixed block and a storage bin are installed, and the side walls of the fixed block are respectively provided with an air inlet and an inlet. The bottom of the fixed block is equipped with a tin nozzle, the top of the fixed block is equipped with a laser fiber optic head, the bottom of the storage bin is provided with a discharge through hole, and the floor is provided with a drop channel connected with the feed channel. The distributing slider driven by the linear drive device is slidably installed. There are positioning holes on the distributing slider, and the cylinder is used to drive the distributing slider to slide, so as to push the solder ball into the exit of the tin nozzle, and then use the laser beam to The tin ball is melted, and the tin ball is ejected from the outlet of the tin nozzle under the pressure of the shielding gas, thereby performing welding.
但是上述装置由于使用激光束焊接后,激光能量被工件吸收,导致工件表面的温度很高,在取出工件时,需要等待一端时间,降低工作效率并且取出时容易烫伤操作人员,此外焊接的过程中若工件表面有杂质,在焊接的过程中容易出现焊渣降低焊接的质量,很难保证工件生产的质量。However, after the above-mentioned device uses laser beam welding, the laser energy is absorbed by the workpiece, resulting in a high temperature on the surface of the workpiece. When taking out the workpiece, it is necessary to wait for a certain period of time, which reduces the work efficiency and is easy to burn the operator when taking it out. In addition, during the welding process If there are impurities on the surface of the workpiece, welding slag will easily appear during the welding process, which will reduce the quality of welding, and it is difficult to ensure the quality of workpiece production.
发明内容Contents of the invention
针对现有技术的不足,本发明提供了一种传感器全自动激光焊接装置,具备降温效果好,生产质量高等优点,解决了现有装置有烫伤风险以及焊接质量不高的问题。Aiming at the deficiencies of the prior art, the present invention provides a sensor automatic laser welding device, which has the advantages of good cooling effect and high production quality, and solves the problems of the existing device's risk of burns and poor welding quality.
为实现上述目的,本发明提供如下技术方案:一种传感器全自动激光焊接装置,包括工作箱,所述工作箱顶面的左右两侧均固定有支撑板,两个所述支撑板的顶面固定有顶板,所述工作箱上设有焊接机构,所述工作箱上设有固定夹持机构,所述工作箱上设有辅助机构;In order to achieve the above object, the present invention provides the following technical solutions: a fully automatic laser welding device for sensors, including a work box, support plates are fixed on the left and right sides of the top surface of the work box, and the top surfaces of the two support plates A top plate is fixed, a welding mechanism is provided on the work box, a fixed clamping mechanism is provided on the work box, and an auxiliary mechanism is provided on the work box;
此外,所述辅助机构包括固定台,所述固定台固定在工作箱的正面,所述固定台的顶面固安装有风机,所述风机的输出端固定有出风管,所述出风管的外表固定有固定块,所述出风管远离风机的一端固定有导风箱,所述导风箱的背面固定有多个喷风头,所述辅助机构还包括固定安装在工作箱背面的抽风机,所述抽风机的输入端固定有抽风管,所述抽风管远离抽风机的一端固定有抽风罩,所述抽风管的外表面固定有多个支撑块,所述抽风机的输出端固定有进风管,所述辅助机构还包括固定在工作箱内底壁背面的收集箱,所述收集箱的右侧设有箱门。In addition, the auxiliary mechanism includes a fixed table, the fixed table is fixed on the front of the work box, the top surface of the fixed table is fixed with a fan, the output end of the fan is fixed with an air outlet pipe, and the air outlet pipe A fixed block is fixed on the outside of the air outlet pipe, an air guide box is fixed on the end of the air outlet pipe away from the fan, and a plurality of spray heads are fixed on the back of the air guide box. The auxiliary mechanism also includes an exhaust fan fixedly installed on the back of the work box. The input end of the exhaust fan is fixed with an exhaust pipe, the end of the exhaust pipe away from the exhaust fan is fixed with an exhaust hood, the outer surface of the exhaust pipe is fixed with a plurality of support blocks, and the output end of the exhaust fan An air inlet pipe is fixed, and the auxiliary mechanism also includes a collection box fixed on the back of the inner bottom wall of the working box, and a box door is provided on the right side of the collection box.
进一步,所述固定块远离出风管的一端与工作箱相固定,所述支撑块远离抽风管的一端与工作箱相固定。Further, the end of the fixing block away from the air outlet pipe is fixed to the working box, and the end of the support block away from the exhaust pipe is fixed to the working box.
进一步,所述工作箱的背面开设有通孔,所述进风管贯穿通孔并延伸至工作箱内部,并与收集箱的顶面相固定。Further, a through hole is opened on the back of the working box, and the air inlet pipe passes through the through hole and extends to the inside of the working box, and is fixed to the top surface of the collecting box.
进一步,所述固定夹持机构包括两个导向杆,两个所述导向杆分别固定在工作箱内壁的左右两侧之间,底部所述导向杆的外表面滑动连接有下齿板,顶部所述导向杆的外表面滑动连接有上齿板,下齿板顶面的右侧固定有支撑架,所述上齿板顶面的左侧以及支撑架的顶面均固定有连接杆,所述连接杆的顶面固定有夹持板,所述固定夹持机构还包括固定安装在工作箱内壁正面的驱动电机,所述驱动电机的输出轴固定有转动杆,所述转动杆的背面固定有齿轮。Further, the fixed clamping mechanism includes two guide rods, the two guide rods are respectively fixed between the left and right sides of the inner wall of the working box, the outer surface of the bottom guide rod is slidably connected with the lower tooth plate, and the top part is The outer surface of the guide rod is slidably connected with an upper tooth plate, the right side of the top surface of the lower tooth plate is fixed with a support frame, the left side of the top surface of the upper tooth plate and the top surface of the support frame are fixed with connecting rods, the The top surface of the connecting rod is fixed with a clamping plate, and the fixed clamping mechanism also includes a driving motor fixedly installed on the front of the inner wall of the working box. The output shaft of the driving motor is fixed with a rotating rod, and the back of the rotating rod is fixed with a gear.
进一步,所述下齿板与上齿板的侧面均开设有方形孔,所述导向杆为矩形杆,两个所述导向杆分别贯穿两个方形孔并与其滑动连接。Further, the sides of the lower tooth plate and the upper tooth plate are provided with square holes, the guide rods are rectangular rods, and the two guide rods respectively pass through the two square holes and are slidably connected to them.
进一步,所述齿轮的顶部和底部分别与上齿板和下齿板相啮合,所述支撑架呈U字形。Further, the top and the bottom of the gear mesh with the upper tooth plate and the lower tooth plate respectively, and the support frame is U-shaped.
进一步,所述工作箱的顶面开设有让位孔,两个所述连接杆均贯穿让位孔并延伸至工作箱的顶面。Further, a relief hole is opened on the top surface of the work box, and the two connecting rods both pass through the relief hole and extend to the top surface of the work box.
进一步,两个所述夹持板相对的一侧均固定有防护垫,两个所述导向杆位于同一垂直平面内。Further, protective pads are fixed on opposite sides of the two clamping plates, and the two guide rods are located in the same vertical plane.
进一步,所述焊接机构包括双轴直线模组,所述双轴直线模组固定安装在顶板的底面,所双轴直线模组的输出端固定有固定板,所述固定板底面的左右两侧均固定安装有电动气缸,两个所述电动气缸底端固定有安装板,所述安装板的底面固定安装有激光焊接装置本体。Further, the welding mechanism includes a biaxial linear module, the biaxial linear module is fixedly installed on the bottom surface of the top plate, the output end of the biaxial linear module is fixed with a fixed plate, and the left and right sides of the bottom surface of the fixed plate Both electric cylinders are fixedly installed, and the bottom ends of the two electric cylinders are fixed with a mounting plate, and the bottom surface of the mounting plate is fixedly mounted with a laser welding device body.
进一步,所述工作箱底面的四个角处均固定有底座,所述激光焊接装置本体位于工作箱的正上方。Further, bases are fixed at the four corners of the bottom surface of the working box, and the laser welding device body is located directly above the working box.
与现有技术相比,本申请的技术方案具备以下有益效果:Compared with the prior art, the technical solution of the present application has the following beneficial effects:
1、该传感器全自动激光焊接装置,设有辅助机构,通过风机吹出冷风,并由出风管输送至喷风头喷出对工件表面进行降温,可快速将工件取下,同时可通过抽风机的抽风作用,通过抽风罩将焊接过程中的焊渣进行清理,避免焊渣影响工件的焊接质量。1. The sensor automatic laser welding device is equipped with an auxiliary mechanism. The cold air is blown out by the fan, and is transported to the air nozzle by the air outlet pipe to cool down the surface of the workpiece, and the workpiece can be quickly removed. At the same time, the exhaust fan can The exhaust function, the welding slag in the welding process is cleaned through the exhaust hood, so as to prevent the welding slag from affecting the welding quality of the workpiece.
2、该传感器全自动激光焊接装置,设有固定夹持机构,通过驱动电机带动齿轮转动,并通过齿轮带动上齿板和下齿板相对或相背移动,从而通过两个夹持板对工件进行夹持固定,进一步提高工件在焊接过程中的稳定性。2. The sensor automatic laser welding device is equipped with a fixed clamping mechanism, which drives the gear to rotate through the drive motor, and drives the upper tooth plate and the lower tooth plate to move relative or opposite to each other through the gear, so that the workpiece can be fixed by the two clamping plates. Clamping and fixing are carried out to further improve the stability of the workpiece during welding.
3,该传感器全自动激光焊接装置,设有焊接机构,通过双轴直线模组和电动气缸可带动激光焊接装置本体对工件进行焊接,实现全自动焊接过程,人力劳动成本低,焊接效率高。3. The sensor automatic laser welding device is equipped with a welding mechanism, which can drive the laser welding device body to weld the workpiece through the biaxial linear module and electric cylinder, realizing the automatic welding process, low labor cost and high welding efficiency.
附图说明Description of drawings
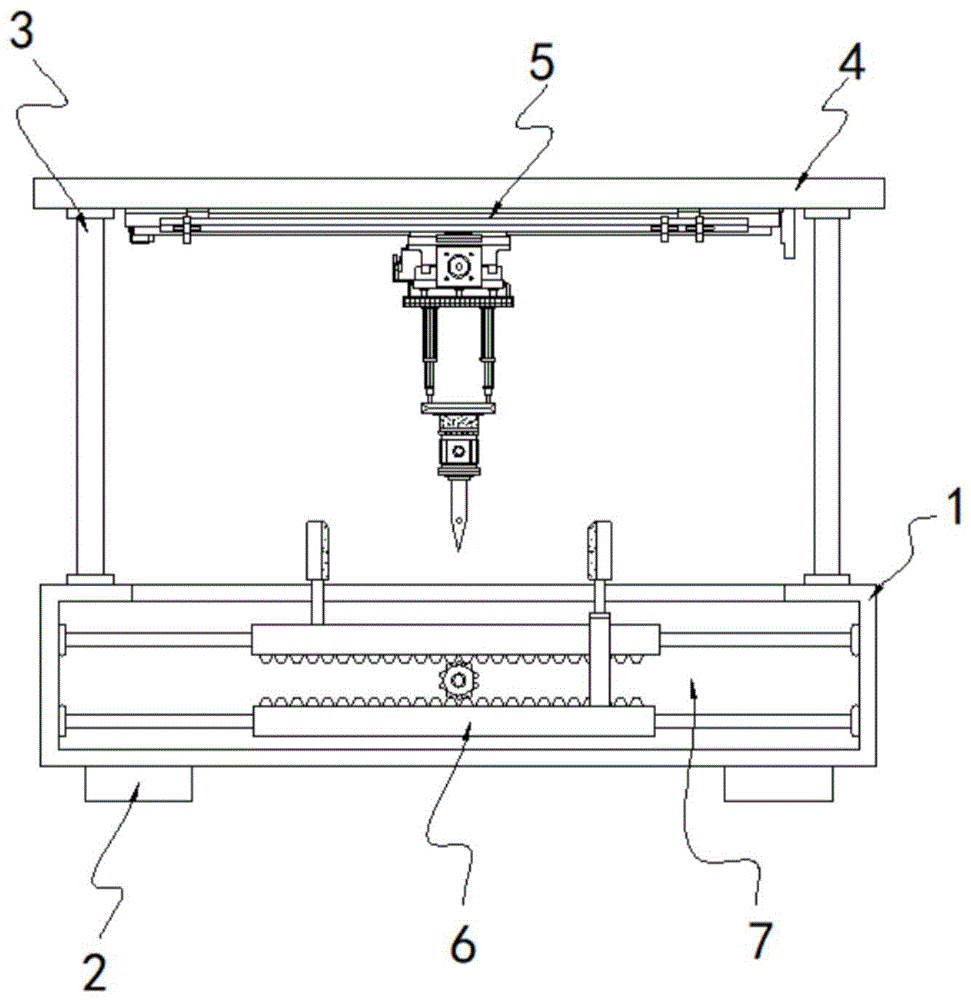
图1为本发明的结构示意图;Fig. 1 is a structural representation of the present invention;
图2为本发明辅助机构的结构示意图;Fig. 2 is the structural representation of auxiliary mechanism of the present invention;
图3为本发明固定夹持机构的结构示意图;Fig. 3 is a schematic structural view of the fixed clamping mechanism of the present invention;
图4为本发明驱动电机和转动杆的连接结构示意图;Fig. 4 is a schematic diagram of the connection structure of the drive motor and the rotating rod of the present invention;
图5为本发明焊接机构的结构示意图。Fig. 5 is a structural schematic diagram of the welding mechanism of the present invention.
图中:1工作箱、2底座、3支撑板、4顶板、5焊接机构、501双轴直线模组、502固定板、503电动气缸、504安装板、505激光焊接装置本体、6固定夹持机构、601导向杆、602下齿板、603上齿板、604支撑架、605连接杆、606夹持板、607驱动电机、608转动杆、609齿轮、7辅助机构、701固定台、702风机、703出风管、704固定块、705导风箱、706喷风头、707抽风机、708抽风管、709抽风罩、710支撑块、711进风管、712收集箱、713箱门。In the figure: 1 working box, 2 base, 3 support plate, 4 top plate, 5 welding mechanism, 501 biaxial linear module, 502 fixed plate, 503 electric cylinder, 504 mounting plate, 505 laser welding device body, 6 fixed clamping Mechanism, 601 guide rod, 602 lower tooth plate, 603 upper tooth plate, 604 support frame, 605 connecting rod, 606 clamping plate, 607 driving motor, 608 rotating rod, 609 gear, 7 auxiliary mechanism, 701 fixed table, 702 fan , 703 air outlet pipe, 704 fixed block, 705 air guide box, 706 air spray head, 707 exhaust fan, 708 exhaust pipe, 709 exhaust hood, 710 support block, 711 air inlet pipe, 712 collection box, 713 box door.
具体实施方式Detailed ways
下面将结合本发明实施例中的附图,对本发明实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本发明保护的范围。The following will clearly and completely describe the technical solutions in the embodiments of the present invention with reference to the accompanying drawings in the embodiments of the present invention. Obviously, the described embodiments are only some, not all, embodiments of the present invention. Based on the embodiments of the present invention, all other embodiments obtained by persons of ordinary skill in the art without making creative efforts belong to the protection scope of the present invention.
请参阅图1,本实施例中的一种传感器全自动激光焊接装置,包括工作箱1,工作箱1的右侧设有现有技术中的合页箱门,便于打开合页箱门清理焊渣,工作箱1顶面的左右两侧均固定有支撑板3,两个支撑板3的顶面固定有顶板4,工作箱1上设有焊接机构5,工作箱1上设有固定夹持机构6,工作箱1上设有辅助机构7。Please refer to Fig. 1, a kind of sensor full-automatic laser welding device in the present embodiment, comprises working
请参阅图2,为了便于提高工作效率以及提高工件的焊接质量,辅助机构7包括固定台701,固定台701固定在工作箱1的正面,固定台701的顶面固安装有风机702,风机702的输出端固定有出风管703,出风管703的外表面固定有固定块704,出风管703远离风机702的一端固定有导风箱705,导风箱705的背面固定有多个喷风头706,辅助机构7还包括固定安装在工作箱1背面的抽风机707,抽风机707的输入端固定有抽风管708,抽风管708远离抽风机707的一端固定有抽风罩709,抽风管708的外表面固定有多个支撑块710,抽风机707的输出端固定有进风管711,辅助机构7还包括固定在工作箱1内底壁背面的收集箱712,收集箱712的右侧设有箱门713。Please refer to Fig. 2, in order to improve work efficiency and improve the welding quality of workpiece,
其中,固定块704远离出风管703的一端与工作箱1相固定,使出风管703在送风的过程中更加稳定,支撑块710远离抽风管708的一端与工作箱1相固定,使抽风管708在清理焊渣的过程中更加稳定,并对抽风管708提供支撑力。Wherein, the end of the
同时,工作箱1的背面开设有通孔,进风管711贯穿通孔并延伸至工作箱1内部,并与收集箱712的顶面相固定,在焊渣清理的过程中,便于将焊渣通过进风管711收集至收集箱712内。At the same time, the back side of the working
请参阅图3-4,为了便于对工件进行固定提高工件焊接过程中的稳定性,固定夹持机构6包括两个导向杆601,两个导向杆601分别固定在工作箱1内壁的左右两侧之间,底部导向杆601的外表面滑动连接有下齿板602,顶部导向杆601的外表面滑动连接有上齿板603,下齿板602顶面的右侧固定有支撑架604,上齿板603顶面的左侧以及支撑架604的顶面均固定有连接杆605,连接杆605的顶面固定有夹持板606,固定夹持机构6还包括固定安装在工作箱1内壁正面的驱动电机607,驱动电机607的输出轴固定有转动杆608,转动杆608的背面固定有齿轮609。Please refer to Figure 3-4, in order to facilitate the fixing of the workpiece and improve the stability of the workpiece welding process, the fixed
此外,下齿板602与上齿板603的侧面均开设有方形孔,导向杆601为矩形杆,两个导向杆601分别贯穿两个方形孔并与其滑动连接,避免上齿板603与下齿板602在导向杆601的外表面转动,在左右移动的过程中保持水平运动。In addition, the sides of the
需要说明的是,齿轮609的顶部和底部分别与上齿板603和下齿板602相啮合,便于通过齿轮609的转动带动下齿板602与上齿板603相对或相背移动,支撑架604呈U字形,下齿板602在左右移动的过程中不会被顶部导向杆601阻挡。It should be noted that the top and bottom of the
可以理解的是,工作箱1的顶面开设有让位孔,两个连接杆605均贯穿让位孔并延伸至工作箱1的顶面,两个连接杆605可带动两个夹持板606相对或相背移动,从而对工件进行固定或解除固定。It can be understood that the top surface of the working
其中,两个夹持板606相对的一侧均固定有防护垫,避免夹持板606的硬度太高剐花工件的外表面,降低其质量,两个导向杆601位于同一垂直平面内,可使上齿板603与下齿板602位于同一垂直平面内,便于齿轮609驱动上齿板603与下齿板602相对或相背移动。Wherein, the opposite sides of the two clamping
请参阅图5,为了便于实现对工件全自动焊接工作,焊接机构5包括双轴直线模组501,可进行左右前后移动,双轴直线模组501固定安装在顶板4的底面,所双轴直线模组501的输出端固定有固定板502,固定板502底面的左右两侧均固定安装有电动气缸503,可实现上下移动,两个电动气缸503底端固定有安装板504,安装板504的底面固定安装有激光焊接装置本体505,通过双轴直线模组501和电动气缸503的配合作用可实现激光焊接装置本体505的全自动焊接工作,提高了焊接的效率和焊接的质量。Please refer to Fig. 5, in order to facilitate the automatic welding of the workpiece, the
最后,工作箱1底面的四个角处均固定有底座2,激光焊接装置本体505位于工作箱1的正上方,便于对工件进行焊接工作。Finally, the four corners of the bottom surface of the working
上述实施例的工作原理为:使用时,可将工件放置在工作箱1的顶面,然后通过驱动电机607带动转动杆608转动,进一步通过齿轮609带动下齿板602与上齿板603向相对的一侧进行移动,下齿板602与上齿板603在相对移动的过程中会带动两个夹持板606一同相对移动,并通过两个夹持板606对工件进行夹持固定,紧接着便可通过双轴直线模组501带动激光焊接装置本体505左右前后移动调整焊接位置,最后便可通过电动气缸503带动激光焊接装置本体505对工件进行自动焊接工作,此外若在焊接过程中有焊渣产生,可启动抽风机707通过抽风管708进行抽风处理,进一步通过抽风罩709将焊渣通过进风管711吸入到收集箱712内,若收集箱712内焊渣收集满以后可打开箱门713将焊渣进行清理,最终当工件焊接完毕后,通过风机702将冷风通过出风管703输送至导风箱705内最后由喷风头706喷出,从而对工件进行快速降温,便于将工件取下开始下一个工件的焊接工作,从而提高工作效率。The working principle of the above embodiment is: when in use, the workpiece can be placed on the top surface of the working
需要说明的是,在本文中,诸如第一和第二等之类的关系术语仅仅用来将一个实体或者操作与另一个实体或操作区分开来,而不一定要求或者暗示这些实体或操作之间存在任何这种实际的关系或者顺序。而且,术语“包括”、“包含”或者其任何其他变体意在涵盖非排他性的包含,从而使得包括一系列要素的过程、方法、物品或者设备不仅包括那些要素,而且还包括没有明确列出的其他要素,或者是还包括为这种过程、方法、物品或者设备所固有的要素。在没有更多限制的情况下,由语句“包括一个……”限定的要素,并不排除在包括所述要素的过程、方法、物品或者设备中还存在另外的相同要素。It should be noted that in this article, relational terms such as first and second are only used to distinguish one entity or operation from another entity or operation, and do not necessarily require or imply that there is a relationship between these entities or operations. There is no such actual relationship or order between them. Furthermore, the term "comprises", "comprises" or any other variation thereof is intended to cover a non-exclusive inclusion such that a process, method, article, or apparatus comprising a set of elements includes not only those elements, but also includes elements not expressly listed. other elements of or also include elements inherent in such a process, method, article, or device. Without further limitations, an element defined by the phrase "comprising a ..." does not exclude the presence of additional identical elements in the process, method, article or apparatus comprising said element.
尽管已经示出和描述了本发明的实施例,对于本领域的普通技术人员而言,可以理解在不脱离本发明的原理和精神的情况下可以对这些实施例进行多种变化、修改、替换和变型,本发明的范围由所附权利要求及其等同物限定。Although the embodiments of the present invention have been shown and described, those skilled in the art can understand that various changes, modifications and substitutions can be made to these embodiments without departing from the principle and spirit of the present invention. and modifications, the scope of the invention is defined by the appended claims and their equivalents.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310611761.XA CN116423047A (en) | 2023-05-29 | 2023-05-29 | A sensor automatic laser welding device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310611761.XA CN116423047A (en) | 2023-05-29 | 2023-05-29 | A sensor automatic laser welding device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN116423047A true CN116423047A (en) | 2023-07-14 |
Family
ID=87087507
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202310611761.XA Withdrawn CN116423047A (en) | 2023-05-29 | 2023-05-29 | A sensor automatic laser welding device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN116423047A (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117564562A (en) * | 2024-01-15 | 2024-02-20 | 河南威猛振动设备股份有限公司 | Welding device with adjustable welding station and welding method |
| CN118527876A (en) * | 2024-06-29 | 2024-08-23 | 浙江汉博汽车传感器有限公司 | A six-axis precision welding machine for sensors |
| CN120962112A (en) * | 2025-08-21 | 2025-11-18 | 湖北吉野房车装备有限公司 | Automatic welding device and welding method for folding ladder |
-
2023
- 2023-05-29 CN CN202310611761.XA patent/CN116423047A/en not_active Withdrawn
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117564562A (en) * | 2024-01-15 | 2024-02-20 | 河南威猛振动设备股份有限公司 | Welding device with adjustable welding station and welding method |
| CN117564562B (en) * | 2024-01-15 | 2024-04-19 | 河南威猛振动设备股份有限公司 | Welding device with adjustable welding station and welding method |
| CN118527876A (en) * | 2024-06-29 | 2024-08-23 | 浙江汉博汽车传感器有限公司 | A six-axis precision welding machine for sensors |
| CN120962112A (en) * | 2025-08-21 | 2025-11-18 | 湖北吉野房车装备有限公司 | Automatic welding device and welding method for folding ladder |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN115922077A (en) | Laser welding machine | |
| CN114559139A (en) | Novel plasma cutting machine that can pinpoint | |
| CN118720319A (en) | An automatic smoke exhaust soldering equipment for controller circuit board production | |
| CN219483646U (en) | Off-line table-board type four-axis plasma cleaning machine | |
| CN121402818A (en) | Water-curtain cooled intelligent laser welding machine and method for preventing fume poisoning | |
| CN216378302U (en) | Quenching device convenient for cleaning waste chips | |
| CN215145258U (en) | Aluminum plate cutting equipment for machining | |
| CN222986011U (en) | A protective device for laser welding machine | |
| CN222754580U (en) | Self-cleaning pressure welding equipment | |
| CN220050397U (en) | Spot welding device for iron painting processing | |
| CN111673293A (en) | A laser cutting equipment with protective structure | |
| CN117655544A (en) | Advertisement making laser engraving device | |
| CN118789132A (en) | Laser cutting equipment for stainless steel processing | |
| CN117983959A (en) | Television backboard laser welding device | |
| CN217019592U (en) | Blowing slag discharging device for machining of machine tool accessories | |
| CN216607579U (en) | A CNC plasma cutting machine with good protective effect | |
| CN116727932A (en) | Aluminum product welding set with heat dissipation function | |
| CN211162298U (en) | Automatic tin soldering machine | |
| CN211991250U (en) | Cutting device is used in block terminal manufacturing | |
| CN220427233U (en) | Welding machine with cleaning component for stretching net | |
| CN220480488U (en) | Circuit board processing welding equipment | |
| CN216829147U (en) | Robot laser welding device | |
| CN223419161U (en) | Lens polishing device for optical instrument production | |
| CN217529677U (en) | Welding device for machining | |
| CN219805499U (en) | Cable welding machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WW01 | Invention patent application withdrawn after publication | ||
| WW01 | Invention patent application withdrawn after publication |
Application publication date: 20230714 |