CN116379891A - A detection method for coaxiality and end-face parallelism of large-aperture serial holes - Google Patents
A detection method for coaxiality and end-face parallelism of large-aperture serial holes Download PDFInfo
- Publication number
- CN116379891A CN116379891A CN202310371600.8A CN202310371600A CN116379891A CN 116379891 A CN116379891 A CN 116379891A CN 202310371600 A CN202310371600 A CN 202310371600A CN 116379891 A CN116379891 A CN 116379891A
- Authority
- CN
- China
- Prior art keywords
- hole
- coaxiality
- parallelism
- serial
- workpiece
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B5/00—Measuring arrangements characterised by the use of mechanical techniques
- G01B5/24—Measuring arrangements characterised by the use of mechanical techniques for measuring angles or tapers; for testing the alignment of axes
- G01B5/25—Measuring arrangements characterised by the use of mechanical techniques for measuring angles or tapers; for testing the alignment of axes for testing the alignment of axes
- G01B5/252—Measuring arrangements characterised by the use of mechanical techniques for measuring angles or tapers; for testing the alignment of axes for testing the alignment of axes for measuring eccentricity, i.e. lateral shift between two parallel axes
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B5/00—Measuring arrangements characterised by the use of mechanical techniques
- G01B5/24—Measuring arrangements characterised by the use of mechanical techniques for measuring angles or tapers; for testing the alignment of axes
- G01B5/25—Measuring arrangements characterised by the use of mechanical techniques for measuring angles or tapers; for testing the alignment of axes for testing the alignment of axes
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E30/00—Energy generation of nuclear origin
- Y02E30/30—Nuclear fission reactors
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- A Measuring Device Byusing Mechanical Method (AREA)
Abstract
Description
技术领域technical field
本发明涉及同轴度和平行度检测技术领域,具体涉及一种大孔径串孔同轴度及端面平行度检测方法。The invention relates to the technical field of coaxiality and parallelism detection, in particular to a method for detecting the coaxiality and end surface parallelism of large-aperture serial holes.
背景技术Background technique
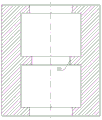
目前在对工件小或者被测工件孔径小的情况下,对工件的同轴度检测和平行度检测采用将被测工件安装在能够转动的物体上,在保证工件中心与转动中心后,转动工件,转动过程中,接触工件的百分表读数发生跳动,根据跳动值得到同轴度情况,但是这种常规方式对于大孔径且中部有串孔的情况的检测存在转动难度大和检测不准确的问题。比如针对含串孔的箱类工件,该类工件结构剖视图如附图1所示,包括工件上下端面的端孔和位于工件内部的串孔,工件的最小孔径在直径450mm左右,工件孔径大,壁厚大,使得工件体积大且重量也大,造成工件转动困难,工件中心找正难度大而存在测量同轴度不准确的问题。At present, when the workpiece is small or the aperture of the measured workpiece is small, the coaxiality detection and parallelism detection of the workpiece adopts the method of installing the measured workpiece on a rotatable object, and rotating the workpiece after ensuring the center of the workpiece and the center of rotation. , during the rotation process, the reading of the dial indicator in contact with the workpiece jumps, and the coaxiality is obtained according to the jump value, but this conventional method has the problems of difficult rotation and inaccurate detection for the detection of large apertures and serial holes in the middle . For example, for box-type workpieces with string holes, the structural cross-sectional view of this type of workpiece is shown in Figure 1, including the end holes on the upper and lower end surfaces of the workpiece and the string holes inside the workpiece. The minimum diameter of the workpiece is about 450 mm in diameter, and the diameter of the workpiece is large. The large wall thickness makes the workpiece bulky and heavy, which makes it difficult to rotate the workpiece, and it is difficult to align the center of the workpiece and there is a problem of inaccurate measurement of coaxiality.
对于这类工件,可以采用“三坐标”检测,“三坐标”检测是检验工件的一种精密测量方法,广泛应用于机械制造业、汽车工业等现代工业中。其优点是结果精确,适用范围广,可以检测几乎所有的形位公差。但是缺点是投入资金极大,操作人员要求专业培训、使用环境要求严格、必须保证应有的配套保障设施、维修保养费用高。For this kind of workpiece, "three-coordinate" detection can be used. "Three-coordinate" detection is a precise measurement method for inspecting workpieces, and is widely used in modern industries such as machinery manufacturing and automobile industry. Its advantages are accurate results, wide application range, and can detect almost all shape and position tolerances. But the disadvantage is that the investment is huge, the operators require professional training, the use environment is strict, the necessary supporting facilities must be guaranteed, and the maintenance cost is high.
发明内容Contents of the invention
本发明意在提供一种大孔径串孔同轴度及端面平行度检测方法,以解决目前针对大孔径且中部存在串孔的工件进行同轴度检测存在的检测难度大和检测成本无法兼顾的问题。The present invention intends to provide a method for detecting the coaxiality and end parallelism of large-diameter serial holes, so as to solve the problem that the current coaxiality detection of workpieces with large apertures and serial holes in the middle is difficult to detect and the detection cost cannot be taken into account. .
为达到上述目的,本发明采用如下技术方案:To achieve the above object, the present invention adopts the following technical solutions:
一种大孔径串孔同轴度及端面平行度检测方法,需要采用检具进行同轴度和平行度的检测,检具包括支撑座,支撑座底部设有两个定位柱和至少两个支撑柱,定位柱的高度高于支撑柱,支撑座上安装有安装架,安装架远离支撑座的一端安装有百分表;A method for detecting the coaxiality and parallelism of large-diameter serial holes requires the use of inspection tools for the detection of coaxiality and parallelism. The inspection tool includes a support seat, and the bottom of the support seat is provided with two positioning columns and at least two supports. The height of the positioning column is higher than that of the supporting column, and a mounting bracket is installed on the supporting base, and a dial indicator is installed on the end of the mounting bracket away from the supporting base;
在对串孔和端孔进行同轴度和平行度的检测时,将支撑座的两个定位柱抵紧在端孔的孔壁上,支撑柱放置在端孔的上端面上,百分表的探头贴在串孔的孔壁上或者端面上,然后带动支撑座移动,使得支撑座的定位柱紧扣工件端孔内壁的同时沿着端孔旋转一圈以上,记录下每圈百分表的跳动最大值。When testing the coaxiality and parallelism of the string hole and the end hole, the two positioning columns of the support seat are pressed against the hole wall of the end hole, the support column is placed on the upper end surface of the end hole, and the dial indicator The probe is attached to the hole wall or end surface of the serial hole, and then drives the support seat to move, so that the positioning column of the support seat is fastened to the inner wall of the workpiece end hole and rotates along the end hole for more than one circle at the same time, record the dial indicator for each circle the maximum jumping value.
本方案的原理及优点是:实际应用时,在需要对带有串孔的工件进行同轴度检测时,让支撑座的两个定位柱同时紧贴在工件端孔的孔壁上,让百分表的探头贴在串孔的孔壁上,检测人员用手拉动支撑座移动,使得支撑座的定位柱紧扣工件端孔内壁的同时沿着端孔旋转,旋转的圈数可以为2圈,3圈,取各圈百分表跳动的最大值,然后计算均值,即为测得的端孔与串孔的同轴度的情况。然后改变百分表探头的作用位置,使得百分表的探头作用在串孔的端面上,同样检测人员带动支撑座的定位柱贴着端孔内壁旋转一圈以上,每圈记录百分表的最大跳动值,之后取所有圈最大跳动值的均值,即为端孔的端面与串孔端面的平行度情况。The principle and advantages of this scheme are: in actual application, when it is necessary to perform coaxiality detection on a workpiece with serial holes, let the two positioning columns of the support seat be closely attached to the hole wall of the workpiece end hole at the same time, so that the hundred The probe of the sub-meter is attached to the hole wall of the serial hole, and the inspector pulls the support seat to move by hand, so that the positioning column of the support seat is tightly fastened to the inner wall of the workpiece end hole and rotates along the end hole. The number of rotations can be 2 circles , 3 circles, take the maximum value of the beating of the dial indicator in each circle, and then calculate the average value, which is the measured coaxiality of the end hole and the string hole. Then change the working position of the dial gauge probe so that the dial gauge probe acts on the end face of the string hole. Similarly, the inspector drives the positioning column of the support seat to rotate more than one circle against the inner wall of the end hole, and records the dial gauge’s position for each circle. The maximum run-out value, and then take the average value of the maximum run-out values of all circles, which is the parallelism between the end face of the end hole and the end face of the string hole.
相比现有技术,本方案无需采用三坐标检测,降低了测试设备成本和测试设备维护成本,相比现有的需要找正被测工件中心和带动工件转动的常规检测方法,本方案不需要对工件进行中心找正也不需要使得大尺寸的工件进行旋转,只需要检测人员手持支撑座,带动支撑座贴着端孔孔壁而绕端孔中心旋转即可实现端孔与串孔的同轴度和平行度测试,测试方式简单、测试成本低,且因不存在工件中心无法找正的问题而极大保证了检测的准确性。Compared with the existing technology, this scheme does not need to use three-coordinate detection, which reduces the cost of testing equipment and maintenance costs of testing equipment. The center alignment of the workpiece does not need to rotate the large-sized workpiece. It only needs the inspector to hold the support seat, drive the support seat to stick to the end hole wall and rotate around the center of the end hole to realize the simultaneous alignment of the end hole and the serial hole. Axiality and parallelism test, the test method is simple, the test cost is low, and the accuracy of the test is greatly guaranteed because there is no problem that the center of the workpiece cannot be aligned.
优选的,作为一种改进,所述同轴度和平行度检测前,先对工件的串孔的尺寸公差和形位公差进行检测,确保串孔孔壁和串孔的上下端面的尺寸公差及形位公差均合格。Preferably, as an improvement, before the detection of the coaxiality and parallelism, the dimensional tolerance and shape and position tolerance of the serial holes of the workpiece are detected to ensure the dimensional tolerances of the serial hole walls and the upper and lower end surfaces of the serial holes and The shape and position tolerances are all qualified.
优选的,作为一种改进,在工件的上端孔与串孔的同轴度和平行度检测完成后,将工件调转180°,使得原本位于工件底部的端孔变为工件顶部的端孔,接着对该调转完成的工件上端孔与串孔的同轴度和平行度采用相同方法进行检测。Preferably, as an improvement, after the detection of the coaxiality and parallelism between the upper end hole and the serial holes of the workpiece is completed, the workpiece is turned 180°, so that the end hole originally located at the bottom of the workpiece becomes the end hole at the top of the workpiece, and then The same method is used to detect the coaxiality and parallelism of the upper end hole and the serial hole of the workpiece after the transfer is completed.
有益效果:采用本方案对上下有端孔,中部有串孔的箱类工件进行同轴度和平行度检测时,以串孔为基准,为保证检测的准确性,需要提前对串孔进行检测,以确保串孔的孔壁、串孔的上下端面的尺寸公差及形位公差均在设计范围内,也即使得串孔处于合格状态后,再行端孔与串孔的同轴度检测及平行度检测。Beneficial effects: when adopting this scheme to detect the coaxiality and parallelism of box workpieces with upper and lower end holes and serial holes in the middle, the serial holes are used as the benchmark. In order to ensure the accuracy of the detection, the serial holes need to be detected in advance , to ensure that the dimensional tolerances and shape and position tolerances of the hole wall of the string hole, the upper and lower end surfaces of the string hole are all within the design range, that is, after the string hole is in a qualified state, the coaxiality detection and inspection of the end hole and the string hole Parallelism detection.
此外,本方案以中间的串孔为基准,既保证了检测过程所采用的安装架无需设置的很长,也即降低了安装架悬臂段的长度,降低悬臂端部百分表不稳定的概率,确保检测的可靠性,同时在大孔径和相对较浅的测量深度下,也能方便检测人员直接读取百分表上的数据。In addition, this scheme is based on the serial hole in the middle, which not only ensures that the installation frame used in the detection process does not need to be set very long, but also reduces the length of the cantilever section of the installation frame and reduces the probability of instability of the dial indicator at the end of the cantilever , to ensure the reliability of the detection, and at the same time, under the large aperture and relatively shallow measurement depth, it is also convenient for the detection personnel to directly read the data on the dial indicator.
优选的,作为一种改进,所述安装架包括连杆一、连杆二和装夹组件,连杆一固定安装在支撑座上,装夹组件的数量为两个,其中一个装夹组件用于实现连杆二与连杆一的连接,另一个装夹组件用于连杆二和百分表的连接,装夹组件能够使得连杆二和连杆一形成的整体长度能够调整,装夹组将能够使得百分表相对连杆二转动和移动。Preferably, as an improvement, the installation frame includes connecting rod one, connecting rod two and a clamping assembly. Realize the connection between connecting
有益效果:通过对安装架的具体结构设计,使得连杆一、连杆二的整体长度可以调整,进而适应不同深度的工件的同轴度和平行度检测。而百分表能够相对连杆二进行转动和移动,使得百分表能够测试更多不同孔径的工件,提高了本方案检测方法的适应性。Beneficial effects: through the specific structural design of the mounting frame, the overall lengths of the first connecting rod and the second connecting rod can be adjusted, thereby adapting to the detection of coaxiality and parallelism of workpieces with different depths. The dial indicator can rotate and move relative to the second connecting rod, so that the dial indicator can test more workpieces with different apertures, which improves the adaptability of the detection method of the scheme.
优选的,作为一种改进,所述装夹组件包括容纳座、锁紧件、U型夹板和套筒,容纳座上设有螺柱,螺柱上螺纹连接着锁紧件;容纳座远离螺柱的一段上设有垂直螺柱轴向的通孔;U型夹板的两个夹片滑动在通孔和螺柱之间,U型夹板的两个夹片之间形成有夹持口,夹持口位于容纳座外侧;套筒套在容纳座带通孔的一段上,套筒上设有正对通孔的条形孔,套筒能够沿容纳座轴向移动,被连接的两个零件一个放置在夹持口上,一个放置在通孔上。Preferably, as an improvement, the clamping assembly includes a receiving seat, a locking piece, a U-shaped splint and a sleeve, the receiving seat is provided with a stud, and the locking piece is threaded on the stud; the receiving seat is far away from the screw A section of the column is provided with a through hole vertical to the axial direction of the stud; the two clips of the U-shaped splint slide between the through hole and the stud, and a clamping opening is formed between the two clips of the U-shaped splint. The holding mouth is located outside the receiving seat; the sleeve is sleeved on the section of the receiving seat with a through hole. The sleeve is provided with a strip hole facing the through hole. The sleeve can move axially along the receiving seat. The two connected parts One is placed on the clamping port and one is placed on the through hole.
有益效果:采用本方案的装夹组件,使得本方案在锁紧件拧紧时,锁紧件抵紧U型夹板的其中一个夹片,使得夹持口夹紧零件,与此同时,容纳座带动通孔内的零件靠近锁紧件,而套筒则在U型夹板的推动下远离锁紧件,使得通孔内的零件被抵紧,也即只需要一个锁紧件的旋拧锁紧动作,就能够使得被连接的两个零件均被夹紧,而在没有锁紧时,两个零件中其中一个能够相对夹持口旋转和升降,一个能够相对通孔旋转和升降,使得两个被连接的零件之间的夹角调节方便。Beneficial effect: the clamping assembly of this scheme is adopted, so that when the locking piece is tightened in this scheme, the locking piece presses against one of the clips of the U-shaped splint, so that the clamping mouth clamps the part, and at the same time, the receiving seat drives The parts in the through hole are close to the locking part, while the sleeve is pushed away from the locking part by the U-shaped splint, so that the parts in the through hole are pressed against each other, that is, only one locking part is needed for the screwing and locking action , so that the two connected parts can be clamped, and when not locked, one of the two parts can be rotated and lifted relative to the clamping port, and the other can be rotated and lifted relative to the through hole, so that the two parts are The angle adjustment between the connected parts is convenient.
优选的,作为一种改进,所述容纳座的外表面为圆柱面。本方案将容纳座的外表面设置为圆柱面,使得U型夹板在未被锁紧件和套筒抵紧前可以绕着容纳座旋转,进一步增加了其中一个零件在锁紧前的自由度,增加了被连接的两个零件之间的相对位置调节范围,方便在同一个安装架上既实现百分表在不同方位的布置,满足不同深度、不同孔径的被测工件的同轴度和平行度检测要求,提高本检具方法的实用性。Preferably, as an improvement, the outer surface of the receiving seat is a cylindrical surface. In this solution, the outer surface of the receiving seat is set as a cylindrical surface, so that the U-shaped splint can rotate around the receiving seat before being pressed by the locking member and the sleeve, which further increases the degree of freedom of one of the parts before locking. The relative position adjustment range between the two connected parts is increased, which facilitates the arrangement of the dial indicator in different directions on the same mounting frame, and satisfies the coaxiality and parallelism of the measured workpieces with different depths and different apertures. Accurate testing requirements, improve the practicability of the checking tool method.
优选的,作为一种改进,所述支撑柱的数量为三个,三个支撑柱的连线形成三角形。Preferably, as an improvement, the number of the support columns is three, and the connecting lines of the three support columns form a triangle.
优选的,作为一种改进,三个支撑柱中,其中一个支撑柱与两个定位柱的距离相等,且剩余两个支撑柱关于该支撑柱对称设置。Preferably, as an improvement, among the three support columns, one of the support columns is equidistant from the two positioning columns, and the remaining two support columns are arranged symmetrically with respect to the support columns.
优选的,作为一种改进,所述定位柱的表面设有淬火层,以提高定位柱的硬度和耐磨性能。Preferably, as an improvement, a quenching layer is provided on the surface of the positioning post to improve the hardness and wear resistance of the positioning post.
优选的,作为一种改进,所述支撑座远离定位柱和支撑柱的端面上安装有拉手,以使得支撑座绕端孔的转动更加方便。Preferably, as an improvement, a handle is installed on the end surface of the support base away from the positioning column and the support column, so that the support base can be rotated around the end hole more conveniently.
附图说明Description of drawings
图1为本发明针对的箱类工件的主视剖视图。Fig. 1 is a front sectional view of a box-like workpiece targeted by the present invention.
图2为本发明实施例一在对工件进行同轴度检测时的主视示意图。Fig. 2 is a schematic front view of the first embodiment of the present invention when the coaxiality detection of the workpiece is performed.
图3为本发明实施例一在对工件进行平行度检测时的主视示意图。Fig. 3 is a schematic front view of the first embodiment of the present invention when the parallelism of the workpiece is detected.
图4为本发明实施例一的仰视图。Fig. 4 is a bottom view of Embodiment 1 of the present invention.
图5为本发明实施例二的检具的三维结构示意图。Fig. 5 is a schematic diagram of the three-dimensional structure of the inspection tool according to the second embodiment of the present invention.
图6为图5在另一视角下的三维结构示意图。FIG. 6 is a schematic diagram of the three-dimensional structure of FIG. 5 at another viewing angle.
图7为本发明实施例二中装夹组件的三维结构示意图。Fig. 7 is a three-dimensional schematic diagram of the clamping assembly in the second embodiment of the present invention.
图8为图7中的装夹组件的爆炸图。Fig. 8 is an exploded view of the clamping assembly in Fig. 7 .
具体实施方式Detailed ways
下面通过具体实施方式进一步详细说明:The following is further described in detail through specific implementation methods:
说明书附图中的附图标记包括:支撑座10、定位柱11、支撑柱12、拉手13、安装架20、百分表30、连杆一1、连杆二2、装夹组件3、容纳座31、锁紧件32、U型夹板33、套筒34、条形孔341、螺柱311、通孔312、夹持口331、串孔100。The reference signs in the drawings of the description include:
实施例一Embodiment one
结合图2和图4所示,一种大孔径串孔同轴度及端面平行度检测方法,需要采用检具进行同轴度和平行度的检测,检具包括支撑座10,支撑座10底部固定有两个定位柱11和至少两个支撑柱12,定位柱11的高度高于支撑柱12,支撑座10上安装有安装架20,安装架20远离支撑座10的一端安装有百分表30,两个定位柱11关于安装架20对称分布。具体地,支撑柱12的数量为三个,三个支撑柱12的连线形成三角形。三个支撑柱12中,其中一个支撑柱12与两个定位柱11的距离相等,且剩余两个支撑柱12关于该支撑柱12对称设置。定位柱11的表面设有淬火层,以提高定位柱11的硬度和耐磨性能。支撑座10远离定位柱11和支撑柱12的端面上安装有拉手13。As shown in Fig. 2 and Fig. 4, a method for detecting the coaxiality and parallelism of the large-diameter serial holes requires the use of inspection tools to detect the coaxiality and parallelism. The inspection tool includes a
一种大孔径串孔100同轴度及端面平行度检测方法,具体如下:A method for detecting the coaxiality and end-face parallelism of 100 large-aperture serial holes, specifically as follows:
步骤一、先对串孔100的尺寸公差和形位公差进行检测,检测合格后才进行步骤二和步骤三。Step 1: firstly inspect the dimensional tolerance and shape tolerance of the
步骤二、上端孔与串孔100的同轴度检测:让支撑座10的两个定位柱11同时紧贴在工件上端孔的孔壁上,支撑柱12放置在上端孔的端面上,调整百分表30相对安装架20的位置,使得百分表30的探头贴在串孔100的孔壁上,检测人员用手拉动支撑座10的拉手13,使得支撑座10的定位柱11紧扣工件端孔内壁的同时沿着上端孔旋转,旋转的圈数可以为2圈或3圈甚至更多圈,取各圈百分表30跳动的最大值,然后取所有圈最大跳动值的均值,即为测得的上端孔与串孔100的同轴度的情况。Step 2: Check the coaxiality of the upper hole and the string hole 100: let the two
步骤三、上端孔与串孔100的平行度检测:使得支撑座10的两个定位柱11同时紧贴在工件上端孔的孔壁上,支撑柱12放置在上端孔的端面上,改变百分表30在安转架上的位置,使得百分表30的探头贴在串孔100的上端面上,检测人员用手拉动支撑座10的拉手13,使得支撑座10的定位柱11紧扣工件端孔内壁的同时沿着端孔旋转,旋转的圈数可以为2圈或3圈,取各圈百分表30跳动的最大值,然后取所有圈最大跳动值的均值,即为测得的零件外端面与串孔100端面的平行度情况。
步骤四、利用吊具将工件调转,使得工件的下端孔位于上方,而已经完成同轴度和平行度检测的上端孔位于底部。Step 4: Turn the workpiece around with a sling so that the lower hole of the workpiece is at the top, and the upper hole that has been tested for coaxiality and parallelism is at the bottom.
步骤五、按照步骤三的操作方法,对调转后的工件的上方端孔与串孔100的平行度进行检测。Step 5. According to the operation method of
步骤六、按照步骤二的操作方法,对调转后的工件的上方端孔与串孔100的同轴度进行检测。Step 6. According to the operation method of
相比现有技术,本实施例无需采用三坐标检测,降低了测试设备成本和测试设备维护成本,相比现有的需要找正被测工件中心和带动工件转动的常规检测方法,本实施例不需要对工件进行中心找正也不需要使得大尺寸的工件进行旋转,只需要检测人员手持支撑座10的拉手13,带动支撑座10贴着端孔孔壁而绕端孔中心旋转即可实现端孔与串孔100的同轴度和平行度测试,测试方式简单、测试成本低,且因不存在工件中心无法找正的问题而极大保证了检测的准确性。Compared with the existing technology, this embodiment does not need to use three-coordinate detection, which reduces the cost of testing equipment and maintenance costs of testing equipment. There is no need to center the workpiece or rotate the large-sized workpiece. It is only necessary for the inspector to hold the
实施例二Embodiment two
结合图5至图8,实施例二在实施例一的基础上对安装架20进行了进一步的改进,具体安装架20的改进如下:5 to 8,
安装架20包括连杆一1、连杆二2和装夹组件3,连杆一1固定安装在支撑座10上,装夹组件3的数量为两个,其中一个装夹组件3用于实现连杆二2与连杆一1的连接,另一个装夹组件3用于连杆二2和百分表30的连接。The mounting
每个装夹组件3均包括容纳座31、锁紧件32、U型夹板33和套筒34,容纳座31上加工有螺柱311,螺柱311上螺纹连接着锁紧件32;容纳座31远离螺柱311的一段上加工有垂直螺柱311轴向的通孔312;U型夹板33的两个夹片滑动在通孔312和螺柱311之间的容纳座31中部一段上,U型夹板33的两个夹片之间形成有夹持口331,夹持口331位于容纳座31外侧;套筒34套在容纳座31带通孔312的一段上,套筒34上加工有正对通孔312的条形孔341,容纳座31与U型夹板33、套筒34配合的外表面呈圆柱面,套筒34能够沿容纳座31轴向移动,被连接的两个零件一个放置在夹持口331上,一个放置在通孔312上。Each clamping
以连杆一1和连杆二2的连接为例,连杆一1放置在夹持口331上,连杆二2放置在容纳座31的通孔312上,当连杆一1、连杆二2的相对位置调整完成后,旋拧锁紧件32,使得锁紧件32抵紧U型夹板33的其中一个夹片,U型夹板33的另一个夹片抵紧套筒34,套筒34抵紧连杆二2,该过程中,U型夹板33受到挤压而使得夹持口331夹紧连杆一1;与此同时,容纳座31带动通孔312内的连杆二2靠近锁紧件32,而套筒34又是在U型夹板33的推动下远离锁紧件32,使得连杆二2被抵紧套筒34和容纳座31的通孔312所挤压,也即只需要一个锁紧件32的旋拧锁紧动作,就能够使得被连接的连杆一1和连杆二2均被夹紧,操作非常简单。Take the connection between connecting rod one 1 and connecting rod two 2 as an example, connecting rod one 1 is placed on the
而在锁紧件32没有锁紧时,两个被夹紧的零件中其中一个能够相对夹持口331旋转和升降,一个能够相对通孔312旋转和升降,同时容纳座31还能够绕U型夹板33进行旋转,使得两个被连接的零件之间的夹角调节方便,保证安装在装夹组件3上的百分表30能够调整到平行度检测盒同轴度检测的方位上,还能确保采用同一个安装架20即能够实现不同深度、不同孔径的被测工件的同轴度和平行度检测要求,提高本检测方法的适用性和实用性。When the locking
以上所述的仅是本发明的实施例,方案中公知的具体技术方案和/或特性等常识在此未作过多描述。应当指出,对于本领域的技术人员来说,在不脱离本发明技术方案的前提下,还可以作出若干变形和改进,这些也应该视为本发明的保护范围,这些都不会影响本发明实施的效果和专利的实用性。本申请要求的保护范围应当以其权利要求的内容为准,说明书中的具体实施方式等记载可以用于解释权利要求的内容。What is described above is only an embodiment of the present invention, and common knowledge such as specific technical solutions and/or characteristics known in the solutions will not be described here too much. It should be pointed out that for those skilled in the art, without departing from the technical solution of the present invention, some modifications and improvements can also be made, which should also be regarded as the protection scope of the present invention, and these will not affect the implementation of the present invention effect and utility of the patent. The scope of protection required by this application shall be based on the content of the claims, and the specific implementation methods and other records in the specification may be used to interpret the content of the claims.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310371600.8A CN116379891B (en) | 2023-04-07 | 2023-04-07 | A method for detecting the coaxiality and end face parallelism of large-diameter perforated holes |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310371600.8A CN116379891B (en) | 2023-04-07 | 2023-04-07 | A method for detecting the coaxiality and end face parallelism of large-diameter perforated holes |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN116379891A true CN116379891A (en) | 2023-07-04 |
| CN116379891B CN116379891B (en) | 2025-12-02 |
Family
ID=86963027
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202310371600.8A Active CN116379891B (en) | 2023-04-07 | 2023-04-07 | A method for detecting the coaxiality and end face parallelism of large-diameter perforated holes |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN116379891B (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117773507A (en) * | 2024-01-26 | 2024-03-29 | 重庆机床(集团)有限责任公司 | Methods to ensure the parallelism between the string holes of the tool holder spindle of the gear hobbing machine and the steel-inlaid guide rails |
| CN119665784A (en) * | 2025-02-06 | 2025-03-21 | 中国船舶集团汾西重工有限责任公司 | Geometric tolerance testing tooling and testing methods |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2003042755A (en) * | 2001-07-31 | 2003-02-13 | Toyota Motor Corp | Centering device and method for measuring coaxiality using the centering device |
| CN201748895U (en) * | 2010-01-04 | 2011-02-16 | 河北理工大学 | Device for measuring coaxiality and runout errors |
| CN204188099U (en) * | 2014-11-17 | 2015-03-04 | 江苏太平洋精锻科技股份有限公司 | Axle class end internal orifice dimension is to bounce gauge |
| CN106643437A (en) * | 2016-09-28 | 2017-05-10 | 中国南方航空工业(集团)有限公司 | Coaxiality measuring device and method for mechanical part |
| RU2623817C1 (en) * | 2016-02-15 | 2017-06-29 | Надежда Николаевна Чигрик | Device for measuring and controlling coaxiality of holes |
| CN207779319U (en) * | 2018-02-06 | 2018-08-28 | 浙江中马传动股份有限公司 | Coaxiality check fixture |
| CN208968521U (en) * | 2018-12-06 | 2019-06-11 | 成都鑫三合机电新技术开发有限公司 | A kind of hole system coaxiality check fixture |
| CN219347630U (en) * | 2023-04-07 | 2023-07-14 | 重庆机床(集团)有限责任公司 | Gauge for detecting coaxiality and end surface parallelism of large-aperture serial holes |
-
2023
- 2023-04-07 CN CN202310371600.8A patent/CN116379891B/en active Active
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2003042755A (en) * | 2001-07-31 | 2003-02-13 | Toyota Motor Corp | Centering device and method for measuring coaxiality using the centering device |
| CN201748895U (en) * | 2010-01-04 | 2011-02-16 | 河北理工大学 | Device for measuring coaxiality and runout errors |
| CN204188099U (en) * | 2014-11-17 | 2015-03-04 | 江苏太平洋精锻科技股份有限公司 | Axle class end internal orifice dimension is to bounce gauge |
| RU2623817C1 (en) * | 2016-02-15 | 2017-06-29 | Надежда Николаевна Чигрик | Device for measuring and controlling coaxiality of holes |
| CN106643437A (en) * | 2016-09-28 | 2017-05-10 | 中国南方航空工业(集团)有限公司 | Coaxiality measuring device and method for mechanical part |
| CN207779319U (en) * | 2018-02-06 | 2018-08-28 | 浙江中马传动股份有限公司 | Coaxiality check fixture |
| CN208968521U (en) * | 2018-12-06 | 2019-06-11 | 成都鑫三合机电新技术开发有限公司 | A kind of hole system coaxiality check fixture |
| CN219347630U (en) * | 2023-04-07 | 2023-07-14 | 重庆机床(集团)有限责任公司 | Gauge for detecting coaxiality and end surface parallelism of large-aperture serial holes |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117773507A (en) * | 2024-01-26 | 2024-03-29 | 重庆机床(集团)有限责任公司 | Methods to ensure the parallelism between the string holes of the tool holder spindle of the gear hobbing machine and the steel-inlaid guide rails |
| CN119665784A (en) * | 2025-02-06 | 2025-03-21 | 中国船舶集团汾西重工有限责任公司 | Geometric tolerance testing tooling and testing methods |
Also Published As
| Publication number | Publication date |
|---|---|
| CN116379891B (en) | 2025-12-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN207635974U (en) | Measure the combined detection tool of gear ring M values and gear ring circular runout | |
| CN116379891B (en) | A method for detecting the coaxiality and end face parallelism of large-diameter perforated holes | |
| CN102042796A (en) | Verticality detection device | |
| CN102183192A (en) | Device and method for detecting symmetry of key groove | |
| CN103615957A (en) | Measuring tool for measuring size of D-shaped head | |
| CN101545749B (en) | Inspection tool for measuring ring groove diameter | |
| CN209559171U (en) | A brake drum inner hole detector | |
| CN219347630U (en) | Gauge for detecting coaxiality and end surface parallelism of large-aperture serial holes | |
| CN111829909A (en) | a hardness tester | |
| CN109798860B (en) | A brake drum inner hole detector | |
| CN207797970U (en) | Cylinder material end holes chamfer detecting device | |
| CN216815310U (en) | Detection tool for detecting space parallelism of bridge parts | |
| CN203869647U (en) | Measuring tool measuring dimension of D-shaped head | |
| CN210321575U (en) | Comprehensive verticality inspection device for miter saw turntable and angle plate assembly | |
| CN213455248U (en) | A workpiece height and flatness detection jig | |
| CN212512835U (en) | Frock suitable for percentage table detects | |
| CN221426496U (en) | Glass inspection equipment | |
| CN102012240A (en) | Universal Test Fixture | |
| CN205718715U (en) | A kind of comparing detection means in pin wheel housing gear pin hole | |
| CN206740050U (en) | A kind of online cubing for detecting cylinder parts end chamfer depth and angle | |
| CN222865797U (en) | Height detection device for inner annular step of product barrel | |
| CN211626414U (en) | Flatness detection device | |
| CN211425258U (en) | Device for detecting steering gear mounting bracket | |
| CN221764332U (en) | End face runout measuring device for cylindrical sleeve parts | |
| CN221976010U (en) | An inner hole coaxiality inspection tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |