CN116352339A - Special-shaped workpiece assembling and welding tool - Google Patents
Special-shaped workpiece assembling and welding tool Download PDFInfo
- Publication number
- CN116352339A CN116352339A CN202111630237.4A CN202111630237A CN116352339A CN 116352339 A CN116352339 A CN 116352339A CN 202111630237 A CN202111630237 A CN 202111630237A CN 116352339 A CN116352339 A CN 116352339A
- Authority
- CN
- China
- Prior art keywords
- bottom plate
- plate
- workpiece
- tooling
- clamping
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K37/00—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass
- B23K37/04—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass for holding or positioning work
- B23K37/0426—Fixtures for other work
- B23K37/0435—Clamps
- B23K37/0443—Jigs
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Landscapes
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Jigs For Machine Tools (AREA)
Abstract
本发明公开了一种异形工件的组对焊接工装,该异形工件包括工件底板,其中工件底板的顶面上垂向平行焊接有多块立板;定义立板的延伸方向为水平横向,立板外壁的对向夹装定位方向为水平纵向;组对焊接工装包括工装底板、滑动内撑单元及顶紧单元,其中工装底板的顶面中部架设异形工件的工件底板,工装底板的顶面两端对向滑动导向连接顶撑在多块立板之间的滑动内撑单元,且工装底板的两侧调节连接有多个对向夹装定位工件底板的顶紧单元。该组对焊接工装可实现工件的快速夹装和快速拆卸,且结构简单,易于实现。
The invention discloses a butt welding tool for a special-shaped workpiece. The special-shaped workpiece includes a workpiece bottom plate, wherein a plurality of vertical plates are welded vertically and parallelly on the top surface of the workpiece bottom plate; The positioning direction of the facing clamping of the outer wall is horizontal and longitudinal; the butt welding tooling includes the tooling bottom plate, the sliding inner support unit and the top tightening unit, wherein the workpiece bottom plate of the special-shaped workpiece is erected in the middle of the top surface of the tooling bottom plate, and the two ends of the top surface of the tooling bottom plate The opposite sliding guides are connected to the sliding inner supporting units supported between the plurality of vertical plates, and the two sides of the tooling base plate are adjusted and connected with a plurality of clamping units oppositely clamping and positioning the workpiece base plate. The set of butt welding tooling can realize quick clamping and quick dismounting of workpieces, and has a simple structure and is easy to realize.
Description
技术领域technical field
本发明涉及工装夹具技术领域,具体为一种异形工件的组对焊接工装。The invention relates to the technical field of tooling fixtures, in particular to a butt welding tooling for special-shaped workpieces.
背景技术Background technique
现有技术中,组对焊接作为平板工件组装为立体工件并焊接加工的定位工装,得到了广泛的使用,但是现有的焊接工装多用于进行工件的外部定位,且焊接加工完成后,工装上的调节夹紧部件需一一旋松,并为工件提供让位,方可由工装内拆除焊接完成的工件,其步骤较为繁琐且调节部件众多,难以保证多次定位的精度及公差的统一。In the prior art, butt welding has been widely used as a positioning tool for assembling flat workpieces into three-dimensional workpieces and welding processing. However, the existing welding tools are mostly used for external positioning of the workpiece, and after the welding process is completed, the tooling The adjustment clamping parts need to be unscrewed one by one, and the workpiece can be provided with a place to remove the welded workpiece from the tooling. The steps are cumbersome and there are many adjustment parts, so it is difficult to ensure the accuracy and tolerance of multiple positioning.
发明内容Contents of the invention
本发明的目的在于克服现有技术的不足之处,提供一种异形工件的组对焊接工装,该组对焊接工装可实现工件的快速夹装和快速拆卸,且结构简单,易于实现。The object of the present invention is to overcome the shortcomings of the prior art and provide a butt welding tool for special-shaped workpieces. The butt welding tool can realize quick clamping and quick disassembly of workpieces, and has a simple structure and is easy to implement.
一种异形工件的组对焊接工装,该异形工件包括工件底板,其中工件底板的顶面上垂向平行焊接有多块立板;定义立板的延伸方向为水平横向,立板外壁的对向夹装定位方向为水平纵向;组对焊接工装包括工装底板、滑动内撑单元及顶紧单元,其中工装底板的顶面中部架设异形工件的工件底板,工装底板的顶面两端对向滑动导向连接顶撑在多块立板之间的滑动内撑单元,且工装底板的两侧调节连接有多个对向夹装定位工件底板的顶紧单元。A butt welding tool for a special-shaped workpiece, the special-shaped workpiece includes a workpiece bottom plate, wherein a plurality of vertical plates are welded vertically and parallel to the top surface of the workpiece bottom plate; The positioning direction of clamping is horizontal and vertical; butt welding tooling includes tooling bottom plate, sliding inner support unit and jacking unit, wherein the workpiece bottom plate of special-shaped workpiece is erected in the middle of the top surface of the tooling bottom plate, and the two ends of the top surface of the tooling bottom plate face sliding guide The sliding inner support unit that is supported between multiple vertical plates is connected, and the two sides of the tooling base plate are adjusted and connected with a plurality of clamping units that clamp and position the workpiece base plate oppositely.
而且,滑动内撑单元包括第一滑座、第二滑座及多个滑道,其中多个滑道均沿立板的延伸方向固设在工装底板的两端,该滑道上分别滑动支撑连接第一滑座及第二滑座;第一滑座及第二滑座的上部均固设有内撑支架,该内撑支架的两侧外壁上穿透连接有多个顶杆及弹簧顶珠;第一滑座的内撑支架上还穿透连接有拉杆,该拉杆的固定端轴向限位连接在内撑支架的内壁上,且拉杆的活动端轴向顶紧连接在立板的外壁上。Moreover, the sliding inner support unit includes a first sliding seat, a second sliding seat and a plurality of slideways, wherein the plurality of slideways are all fixed on both ends of the tooling bottom plate along the extending direction of the vertical plate, and the slideways respectively support and connect The first sliding seat and the second sliding seat; the upper parts of the first sliding seat and the second sliding seat are fixed with inner support brackets, and the outer walls of both sides of the inner support bracket are penetrated and connected with a plurality of ejector rods and spring top beads; The inner support bracket of the first sliding seat is also penetrated and connected with a pull rod, the fixed end of the pull rod is axially limited and connected to the inner wall of the inner support bracket, and the movable end of the pull rod is axially tightly connected to the outer wall of the vertical plate .
而且,顶紧单元包括水平纵向设置的一组L形定位板,水平横向设置的端头卡板,以及多个水平纵向设置的螺纹顶撑组件;L形定位板的底面与工装底板固定连接,L型定位板的底部侧面夹装定位在工件底板的侧壁上,L型定位板的上部侧面配合顶撑在立板的侧壁上;端头卡板固设在工装底板上,该端头卡板的底部侧面配合支撑在工件底板的侧壁上,端头卡板的中部扣装压合在工件底板的顶面上;螺纹顶撑组件调节连接在工装底板上,该螺纹顶撑组件的顶撑端配合顶压在工件底板的侧壁上。Moreover, the jacking unit includes a group of L-shaped positioning plates arranged horizontally and vertically, end clamping plates arranged horizontally and horizontally, and a plurality of threaded supporting components arranged horizontally and vertically; the bottom surface of the L-shaped positioning plate is fixedly connected with the tooling bottom plate, The bottom side of the L-shaped positioning plate is clamped and positioned on the side wall of the workpiece bottom plate, and the upper side of the L-shaped positioning plate is matched with the top support on the side wall of the vertical plate; the end clamping plate is fixed on the tooling bottom plate. The bottom side of the clamping plate is matched and supported on the side wall of the workpiece bottom plate, and the middle part of the end clamping plate is fastened and pressed on the top surface of the workpiece bottom plate; the threaded support assembly is adjusted and connected to the tooling base plate, and the threaded support assembly The supporting end cooperates and presses on the side wall of the workpiece bottom plate.
本发明的优点和技术效果是:Advantage and technical effect of the present invention are:
本发明的一种异形工件的组对焊接工装,通过工装底板提供工件底板的平面支撑,并且为滑动内撑单元及顶紧单元提供定位基准,其中滑动内撑单元用于内撑连接在立板之间,由第一滑座和第二滑座分别滑动插接在立板间隙的两端,便于焊接完成后为工件拆出工装提供快速让位。并且,顶紧单元的L形定位板可沿水平纵向定位夹装工件底板,由端头卡板于水平横向定位工装底板,最后由多个平行设置的螺纹顶撑组件以水平纵向配合顶撑在工件底板的侧壁上,以此多点定位的顶紧单元于外部支撑定位工件。The butt welding tool for special-shaped workpieces of the present invention provides plane support for the workpiece bottom plate through the bottom plate of the tooling, and provides a positioning reference for the sliding inner support unit and the jacking unit, wherein the sliding inner support unit is used for connecting the inner support to the vertical plate Between them, the first sliding seat and the second sliding seat are respectively slidably inserted into the two ends of the gap of the vertical plate, which is convenient to provide a quick way for the workpiece to be removed from the tooling after the welding is completed. Moreover, the L-shaped positioning plate of the clamping unit can position the bottom plate of the clamped workpiece in the horizontal and longitudinal direction, and the tooling bottom plate can be positioned in the horizontal and transverse direction by the end clamping plate, and finally the support is supported by a plurality of threaded supporting components arranged in parallel in a horizontal and longitudinal direction. On the side wall of the workpiece bottom plate, the clamping unit with multi-point positioning is used to support and position the workpiece on the outside.
附图说明Description of drawings
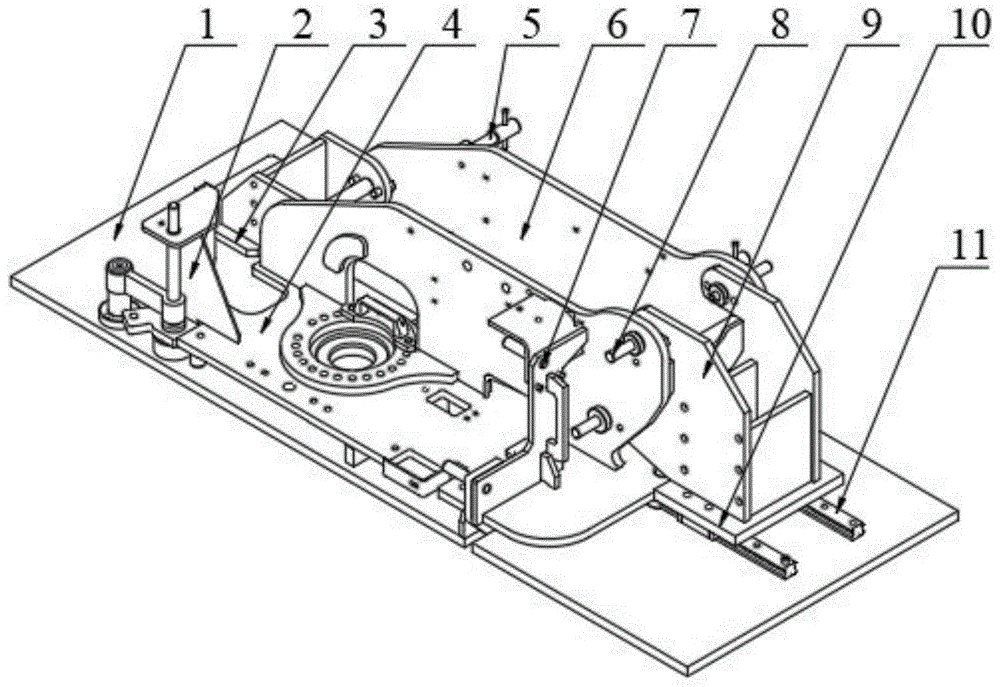
图1为本发明的立体结构示意图;Fig. 1 is the three-dimensional structure schematic diagram of the present invention;
图2为本发明的俯视图;Fig. 2 is the top view of the present invention;
图3为本发明的侧视图;Fig. 3 is a side view of the present invention;
图中:1-工装底板;2-端头卡板;3-第二滑座;4-工件底板;5-螺纹顶撑组件;6-立板;7-L形定位板;8-拉杆;9-内撑支架;10-第一滑座;11-滑道;12-顶杆;13-弹簧顶珠。In the figure: 1-tooling bottom plate; 2-end clamping plate; 3-second slide seat; 4-workpiece bottom plate; 9-inner support bracket; 10-the first sliding seat; 11-sliding way; 12-ejector rod; 13-spring top ball.
具体实施方式Detailed ways
为能进一步了解本发明的内容、特点及功效,兹例举以下实施例,并配合附图详细说明如下。需要说明的是,本实施例是描述性的,不是限定性的,不能由此限定本发明的保护范围。In order to further understand the content, characteristics and effects of the present invention, the following examples are given, and detailed descriptions are given below with reference to the accompanying drawings. It should be noted that this embodiment is descriptive, not restrictive, and cannot thereby limit the protection scope of the present invention.
一种异形工件的组对焊接工装,该异形工件包括工件底板4,其中工件底板的顶面上垂向平行焊接有多块立板6;定义立板的延伸方向为水平横向,立板外壁的对向夹装定位方向为水平纵向;组对焊接工装包括工装底板1、滑动内撑单元及顶紧单元,其中工装底板的顶面中部架设异形工件的工件底板,工装底板的顶面两端对向滑动导向连接顶撑在多块立板之间的滑动内撑单元,且工装底板的两侧调节连接有多个对向夹装定位工件底板的顶紧单元。A butt welding tool for special-shaped workpieces, the special-shaped workpiece includes a
而且,滑动内撑单元包括第一滑座10、第二滑座3及多个滑道11,其中多个滑道均沿立板的延伸方向固设在工装底板的两端,该滑道上分别滑动支撑连接第一滑座及第二滑座;第一滑座及第二滑座的上部均固设有内撑支架9,该内撑支架的两侧外壁上穿透连接有多个顶杆12及弹簧顶珠13;第一滑座的内撑支架上还穿透连接有拉杆8,该拉杆的固定端轴向限位连接在内撑支架的内壁上,且拉杆的活动端轴向顶紧连接在立板的外壁上。Moreover, the sliding inner support unit includes a
而且,顶紧单元包括水平纵向设置的一组L形定位板7,水平横向设置的端头卡板2,以及多个水平纵向设置的螺纹顶撑组件5;L形定位板的底面与工装底板固定连接,L型定位板的底部侧面夹装定位在工件底板的侧壁上,L型定位板的上部侧面配合顶撑在立板的侧壁上;端头卡板固设在工装底板上,该端头卡板的底部侧面配合支撑在工件底板的侧壁上,端头卡板的中部扣装压合在工件底板的顶面上;螺纹顶撑组件调节连接在工装底板上,该螺纹顶撑组件的顶撑端配合顶压在工件底板的侧壁上。Moreover, the tightening unit includes a group of L-
另外,本发明优选的,拉杆、顶杆、弹簧顶珠及螺纹顶撑组件均采用现有技术中的成熟产品,其顶撑定位方式均采用现有技术中的成熟技术手段。In addition, preferably in the present invention, the tie rods, ejector rods, spring top beads and threaded support components are all mature products in the prior art, and the support positioning methods are all mature technical means in the prior art.
为了更清楚地说明本发明的具体实施方式,下面提供一种实施例:In order to illustrate the specific implementation of the present invention more clearly, a kind of embodiment is provided below:
本发明的一种异形工件的组对焊接工装,定位工件时需先将工件底板放置在工装底板上,放置过程中应保证工件底板的两侧由L形定位板夹装定位,工件底板的一端由端口卡板卡接限位;而后拖行第一滑座至预定位置,在第一滑座上固定安装立板,并且立板外部由L形定位板对向夹紧,最后向两个立板中部推入第二滑座并拧紧螺纹顶撑组件,即可实现工件的多点定位及组对焊接定位功能。焊接完成后仅需拆除第一滑座与立板的固定连接,而后背向滑动第一滑座与第二滑座,并旋松螺纹顶撑组件,边便可由工装底板上先平推再上升进而由工装内整体取出焊接完成的工件In the butt welding tooling for special-shaped workpieces of the present invention, when positioning the workpieces, the base plate of the workpiece needs to be placed on the base plate of the tooling first. During the placement process, the two sides of the base plate of the workpiece should be clamped and positioned by the L-shaped positioning plate, and one end of the base plate of the workpiece should be positioned. The limit is clamped by the port clamping plate; then the first sliding seat is dragged to the predetermined position, the vertical plate is fixedly installed on the first sliding seat, and the outside of the vertical plate is clamped by the L-shaped positioning plate, and finally the two vertical The middle part of the plate is pushed into the second sliding seat and the threaded support assembly is tightened to realize the multi-point positioning of the workpiece and the butt welding positioning function. After the welding is completed, it is only necessary to remove the fixed connection between the first sliding seat and the vertical plate, then slide the first sliding seat and the second sliding seat backwards, and loosen the threaded top support assembly, and the side can be pushed flat by the tooling base plate and then raised Then take out the welded workpiece as a whole from the tooling
最后,本发明的未述之处均采用现有技术中的成熟产品及成熟技术手段。Finally, the unrecited parts of the present invention all adopt mature products and mature technical means in the prior art.
应当理解的是,对本领域普通技术人员来说,可以根据上述说明加以改进或变换,而所有这些改进和变换都应属于本发明所附权利要求的保护范围。It should be understood that those skilled in the art can make improvements or changes based on the above description, and all these improvements and changes should belong to the protection scope of the appended claims of the present invention.
Claims (3)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111630237.4A CN116352339A (en) | 2021-12-28 | 2021-12-28 | Special-shaped workpiece assembling and welding tool |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111630237.4A CN116352339A (en) | 2021-12-28 | 2021-12-28 | Special-shaped workpiece assembling and welding tool |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN116352339A true CN116352339A (en) | 2023-06-30 |
Family
ID=86926151
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202111630237.4A Pending CN116352339A (en) | 2021-12-28 | 2021-12-28 | Special-shaped workpiece assembling and welding tool |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN116352339A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119347264A (en) * | 2024-10-31 | 2025-01-24 | 中国兵器工业集团江山重工研究院有限公司 | A welding tool for special-shaped workpiece and use method thereof |
-
2021
- 2021-12-28 CN CN202111630237.4A patent/CN116352339A/en active Pending
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119347264A (en) * | 2024-10-31 | 2025-01-24 | 中国兵器工业集团江山重工研究院有限公司 | A welding tool for special-shaped workpiece and use method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN205464955U (en) | Connecting pipe combination welding jig in motorcycle frame | |
| CN210756086U (en) | Sheet welding fixture | |
| CN103600192A (en) | Welding fixture for urban rail vehicle traction beams | |
| CN213163840U (en) | Right-angle welding processing tool | |
| WO2018223603A1 (en) | New three-linkage-type fully automated steel needle bending machine | |
| CN204546045U (en) | A kind of tiling vertical vehicle machining mould | |
| CN208019823U (en) | Motor train unit gate material clamp for machining | |
| CN209303992U (en) | Scooter cushion welding fixture | |
| CN111014486A (en) | Taper shrinking machine clamping mechanism | |
| CN210476057U (en) | Steel welding auxiliary assembly | |
| CN104972258B (en) | The welding positioning tool of arc plate | |
| CN204221263U (en) | Chain-linked conveyer track girder assembly welding frock | |
| CN103521991A (en) | Horizontal position welding clamping device for workpiece to be welded | |
| CN105479071A (en) | Locating and welding tool of dust remover blowing pipe | |
| CN217253959U (en) | Group butt welding frock of special-shaped workpiece | |
| CN216097190U (en) | Auxiliary welding device for submerged AGV shell | |
| CN211072226U (en) | A high-frequency welding system for side wall processing | |
| CN209902532U (en) | Last tower welding frock in solar rack | |
| CN215548148U (en) | An ABS installation tool | |
| CN205271279U (en) | Dust remover jetting pipe fixed -position welding frock | |
| CN205501112U (en) | A pipe welding fixture | |
| CN208758900U (en) | A kind of nut-welding fixture of backrest connecting plate | |
| CN205325077U (en) | Lower scaffold weldment frock | |
| CN218611323U (en) | A Stamping Die That Can Avoid Abnormal Detachment of Processed Parts | |
| CN218744629U (en) | Round steel upsetting device capable of clamping and positioning |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| WD01 | Invention patent application deemed withdrawn after publication | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20230630 |