CN116214074A - A Machining Method of Small-diameter Super-deep Hole - Google Patents
A Machining Method of Small-diameter Super-deep Hole Download PDFInfo
- Publication number
- CN116214074A CN116214074A CN202310458147.4A CN202310458147A CN116214074A CN 116214074 A CN116214074 A CN 116214074A CN 202310458147 A CN202310458147 A CN 202310458147A CN 116214074 A CN116214074 A CN 116214074A
- Authority
- CN
- China
- Prior art keywords
- drill bit
- hole
- drill
- drilled
- diameter
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P13/00—Making metal objects by operations essentially involving machining but not covered by a single other subclass
- B23P13/02—Making metal objects by operations essentially involving machining but not covered by a single other subclass in which only the machining operations are important
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23B—TURNING; BORING
- B23B35/00—Methods for boring or drilling, or for working essentially requiring the use of boring or drilling machines; Use of auxiliary equipment in connection with such methods
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23B—TURNING; BORING
- B23B51/00—Tools for drilling machines
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Drilling Tools (AREA)
Abstract
本发明公开一种小直径超深孔的加工方法,采用两边对钻的方法,加工步骤如下:第一步用小于预钻孔孔径3‑4mm钨钢铣刀螺旋加工孔深30%‑40%;第二步采用与预钻孔孔径相同的深孔钻头一,深孔钻头一长度为预钻孔孔深的17%,钻至15%孔深;第三步采用与预钻孔孔径相同的深孔钻头二钻至47%孔深;第四步采用与预钻孔孔径相同的深孔钻头三,钻至50%孔深;所述钻头三包括钻尖,所述钻尖的下部与平面部分相连,钻尖的侧部设置排屑槽一,平面部分设置排屑槽二,排屑槽二与钻头本身的排屑槽相连;第五步,采用同样的方法加工另一面。本发明的优点是:借助于钻尖的定位,克服了对钻时,后钻的钻头易发生断裂的现象,保证钻头从另一面钻过来时候的接刀准确。

The invention discloses a processing method for a small-diameter ultra-deep hole, which adopts the method of counter-drilling on both sides, and the processing steps are as follows: the first step is to use a tungsten steel milling cutter with a diameter smaller than the pre-drilled hole of 3-4mm to spirally process the hole depth by 30%-40% ; The second step adopts the same deep hole drill bit 1 with the pre-drilled hole diameter, and the length of the deep hole drill bit 1 is 17% of the pre-drilled hole depth, and drills to 15% hole depth; the third step adopts the same with the pre-drilled hole diameter The deep hole drill bit 2 is drilled to 47% of the hole depth; the fourth step adopts the deep hole drill bit 3 identical with the pre-drilled hole diameter, drilled to 50% of the hole depth; the drill bit 3 includes a drill point, and the bottom of the drill point and the The parts are connected, the side of the drill tip is provided with the chip flute 1, and the plane part is provided with the chip flute 2, and the chip flute 2 is connected with the chip flute of the drill itself; the fifth step is to process the other side in the same way. The invention has the advantages of: by means of the positioning of the drill point, the phenomenon that the drill bit of the rear drill is prone to breakage is overcome when the drill is aligned, and the drill bit is accurately connected when the drill bit is drilled from the other side.
Description
技术领域technical field
本发明涉及机械领域,具体是一种长细孔的加工方法。The invention relates to the field of machinery, in particular to a processing method for long fine holes.
背景技术Background technique
长细孔一直是一个比较棘手的机械加工问题,尤其是孔深与孔径之比超过100的超深孔更是如此。为解决上述问题,人们借助于精密治具的准确定位,从孔的两端相向钻孔,但后钻的钻头钻至孔深的一半时,会发生钻头断裂;这是因为,随着孔深的增加,钻头不可避免的振动会带来钻头与孔壁的接触,而该接触增加了转动的阻力,该阻力形成一种扭矩,如果钻头的驱动力较大,则所述扭矩会造成钻头的断裂。Long and thin holes have always been a difficult machining problem, especially for ultra-deep holes with a ratio of hole depth to hole diameter exceeding 100. In order to solve the above problems, with the help of accurate positioning of precision jigs, people drill holes from opposite ends of the hole, but when the drill bit drilled after drilling reaches half of the hole depth, the drill bit will break; this is because, with the depth of the hole The inevitable vibration of the drill bit will bring the drill bit into contact with the hole wall, and this contact increases the resistance to rotation, which forms a torque. If the driving force of the drill bit is large, the torque will cause the drill bit to rotate. fracture.
发明内容Contents of the invention
为解决上述技术问题,本发明的目的是提供一种小直径超深孔的加工方法,采用两边对钻的方法,其中一面的加工步骤如下:In order to solve the above-mentioned technical problems, the purpose of this invention is to provide a processing method for small-diameter ultra-deep holes, which adopts the method of drilling on both sides, and the processing steps of one side are as follows:
第一步,用小于预钻孔孔径3-4mm钨钢铣刀螺旋加工孔深30%-40%,保证后面用深孔钻头钻孔时钻头不会钻偏;The first step is to use a tungsten steel milling cutter with a diameter of 3-4mm smaller than the pre-drilled hole to helically process the hole depth by 30%-40%, so as to ensure that the drill bit will not deviate when drilling with a deep hole drill bit;
第二步,采用与预钻孔孔径相同的深孔钻头一,深孔钻头一长度为预钻孔孔深的17%,钻至15%孔深,机床转速500转/分,进给50mm/分,每次钻深2mm抬刀,这样加工防止铁屑排不出来导致钻头抱死,断掉,另外钻头太深冷却液加不进也会导致钻头高温会造成孔内光洁度超公差;The second step adopts the same deep
第三步,采用与预钻孔孔径相同的深孔钻头二,深孔钻头二长度为预钻孔孔深的48%,钻至47%孔深;机床转速650转/分,进给30mm/分,每次钻深2mm抬刀;The third step is to adopt the same deep
第四步,采用与预钻孔孔径相同的深孔钻头三,深孔钻头三长度为预钻孔孔深的51%,钻至50%孔深;The fourth step is to adopt the same deep
所述钻头三包括钻尖,所述钻尖的下部与平面部分相连,钻尖的侧部设置排屑槽一,平面部分设置排屑槽二,排屑槽二与钻头本身的排屑槽相连;The
第五步,采用同样的方法加工另一面,直至两个孔钻通。The fifth step is to use the same method to process the other side until the two holes are drilled through.
所述钻尖为45度锥角。The drill tip has a 45 degree cone angle.
所述钻尖根部的直径为预钻孔孔径的三分之一。The diameter of the root of the drill point is one-third of the diameter of the pre-drilled hole.
本发明的优点是:借助于钻尖的定位,克服了对钻时,后钻的钻头易发生断裂的现象,保证钻头从另一面钻过来时候的接刀准确。The invention has the advantages of: by means of the positioning of the drill point, the phenomenon that the drill bit of the rear drill is prone to breakage is overcome when the drill is aligned, and the drill bit is accurately connected when the drill bit is drilled from the other side.
附图说明Description of drawings
图1为深孔钻头三的结构示意图;Fig. 1 is the structural representation of deep
图2为图1的A-A位置剖视图;Fig. 2 is the A-A position sectional view of Fig. 1;
图3为图1的B位置放大示意图;Fig. 3 is an enlarged schematic diagram of position B in Fig. 1;
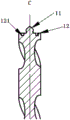
图4为图2的C位置放大示意图;Fig. 4 is an enlarged schematic diagram of position C in Fig. 2;
图5为深孔钻头三的立体示意图;Fig. 5 is the three-dimensional schematic view of deep hole drill bit three;
图6为现有技术钻头对钻时的示意图;Fig. 6 is the schematic diagram when prior art drill bit drills;
图7为本发明的钻头对钻时的示意图。Fig. 7 is a schematic diagram of the drill bit of the present invention when drilling.
具体实施方式Detailed ways
下面结合附图具体说明本发明,如图所示,孔深与孔径之比超过100的超深孔,在钻孔时,刀具路径中的某些点对刀具施加过大的力,从而导致震动。如果该振动导致钻头与孔壁接触,则产生一个抗拒钻杆转动的扭矩,如果扭矩过大,则会使得钻头断裂;为解决上述技术问题,本发明的方案是:The present invention will be described in detail below in conjunction with the accompanying drawings. As shown in the figure, for an ultra-deep hole with a ratio of hole depth to hole diameter exceeding 100, when drilling, certain points in the tool path exert excessive force on the tool, resulting in vibration . If the vibration causes the drill bit to contact the hole wall, a torque that resists the rotation of the drill rod will be produced, and if the torque is too large, the drill bit will break; in order to solve the above technical problems, the solution of the present invention is:
采用两边对钻的方法,其中一面的加工步骤如下:Using the method of drilling on both sides, the processing steps of one side are as follows:
第一步,用小于预钻孔孔径3-4mm钨钢铣刀螺旋加工孔深30%-40%,保证后面用深孔钻头钻孔时钻头不会钻偏;The first step is to use a tungsten steel milling cutter with a diameter of 3-4mm smaller than the pre-drilled hole to helically process the hole depth by 30%-40%, so as to ensure that the drill bit will not deviate when drilling with a deep hole drill bit;
第二步,采用与预钻孔孔径相同的深孔钻头一,深孔钻头一长度为预钻孔孔深的17%,钻至15%孔深,机床转速500转/分,进给50mm/分,每次钻深2mm抬刀,这样加工防止铁屑排不出来导致钻头抱死,断掉,另外钻头太深冷却液加不进也会导致钻头高温会造成孔内光洁度超公差;The second step adopts the same deep
第三步,采用与预钻孔孔径相同的深孔钻头二,深孔钻头二长度为预钻孔孔深的48%,钻至47%孔深;机床转速650转/分,进给30mm/分,每次钻深2mm抬刀;The third step is to adopt the same deep
第四步,采用与预钻孔孔径相同的深孔钻头三,深孔钻头三长度为预钻孔孔深的51%,钻至50%孔深;The fourth step is to adopt the same deep
所述钻头三包括钻尖11,所述钻尖的下部与平面12部分相连,钻尖的侧部设置排屑槽一111,平面部分设置排屑槽二121,排屑槽二121与钻头本身的排屑槽4相连;The drill bit three includes a
第五步,采用同样的方法加工另一面,直至两个孔钻通。The fifth step is to use the same method to process the other side until the two holes are drilled through.
所述钻尖为45度锥角。The drill tip has a 45 degree cone angle.
所述钻尖根部的直径为预钻孔孔径的三分之一。The diameter of the root of the drill point is one-third of the diameter of the pre-drilled hole.
采用本发明的方法加工可以保证孔内粗糙度0.8以上,预钻孔孔径公差在正负0.05之内。Adopting the processing method of the invention can ensure that the roughness in the hole is above 0.8, and the tolerance of the pre-drilled hole diameter is within plus or minus 0.05.
本发明的原理是;现有技术钻头1仅仅是一个锥形的钻尖11,钻尖及钻杆上设置排屑槽;当采用对钻的方式时,预先将孔2的一半钻完,然后从对侧开始钻另外一半;而预先钻完一半留下的金属3具有一个锥形部21,当钻尖钻该位置时,很快钻尖形成“悬空”状态,由于没有钻尖的定位作用,钻头无法克服钻头的径向振动,钻头就会与孔壁接触,造成阻力增大,进而钻头扭断经常发生。The principle of the present invention is; the prior
而采用本发明的深孔钻头三结构,则钻头的钻尖首先会与钻完孔的圆柱形空间22接触,该圆柱形空间限制了钻尖的径向移动,进而保证了钻头不会与孔壁侧面的接触,克服了现有技术经常发生的钻头断裂现象。And adopt three structures of deep-hole drill bit of the present invention, then the drill point of drill bit at first can contact with the
Claims (3)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310458147.4A CN116214074A (en) | 2023-04-26 | 2023-04-26 | A Machining Method of Small-diameter Super-deep Hole |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310458147.4A CN116214074A (en) | 2023-04-26 | 2023-04-26 | A Machining Method of Small-diameter Super-deep Hole |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN116214074A true CN116214074A (en) | 2023-06-06 |
Family
ID=86582883
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202310458147.4A Pending CN116214074A (en) | 2023-04-26 | 2023-04-26 | A Machining Method of Small-diameter Super-deep Hole |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN116214074A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119525548A (en) * | 2024-12-20 | 2025-02-28 | 陕西法士特汽车传动集团有限责任公司 | A small-diameter intermittent deep hole processing technology |
| WO2025200182A1 (en) * | 2024-03-27 | 2025-10-02 | 广州广合科技股份有限公司 | Laser pre-drilling and mechanical drilling machining method |
-
2023
- 2023-04-26 CN CN202310458147.4A patent/CN116214074A/en active Pending
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2025200182A1 (en) * | 2024-03-27 | 2025-10-02 | 广州广合科技股份有限公司 | Laser pre-drilling and mechanical drilling machining method |
| CN119525548A (en) * | 2024-12-20 | 2025-02-28 | 陕西法士特汽车传动集团有限责任公司 | A small-diameter intermittent deep hole processing technology |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN101389432B (en) | Nonaxisymmetrical blade drill | |
| CN204262495U (en) | Dual boot is to deep hole reamer | |
| US10195675B2 (en) | Twist drill with unequal flute spacing and unequal relief angles | |
| CN102294569A (en) | Processing technic of small-diameter thin-wall deep-hole high-accuracy part and special grinding tool applied to same | |
| CN201735837U (en) | Tool fixture assembly capable of adjusting depth of step drill | |
| CN118215551A (en) | Combination tool for drilling and deburring | |
| CN109262206B (en) | Method for machining oil hole of medium-high speed crankshaft | |
| CN220178193U (en) | A tool for processing the joint hole of the column head of the live column of the hydraulic support | |
| CN106584030A (en) | Machining method for small-diameter positioning pin hole | |
| CN102198527B (en) | Method for correcting eccentricity of drill type deep hole | |
| CN204545510U (en) | Be convenient to the drill bit of chip removal | |
| CN204603416U (en) | Z-shaped drilling and milling head | |
| CN204221057U (en) | J type seamed edge correction straight fluted drill | |
| CN103692003B (en) | Auger bit with highly-spiral land | |
| CN104439432A (en) | J-shaped seamed edge correction auger bit | |
| KR101822517B1 (en) | Step drill bit | |
| CN216990021U (en) | A solid carbide deep hole drill | |
| JP2003266223A (en) | Deep hole processing method and drill for processing deep hole | |
| CN219900366U (en) | Drill bit for two-side opposite drilling of small-diameter ultra-deep hole | |
| CN204194895U (en) | A kind of multi-state spiral bit | |
| CN206588386U (en) | A kind of quasi- core bore target drill of processing precise metalwork | |
| CN203711944U (en) | Durable drill | |
| CN217647565U (en) | A drill that can process internal and external chamfering and deburr | |
| JP2005153077A (en) | Method for making deep hole | |
| CN208913162U (en) | For deep hole processing taper blind hole and the boring cutter at clear bottom |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination |