CN115870224A - Appearance detection system for breath card - Google Patents
Appearance detection system for breath card Download PDFInfo
- Publication number
- CN115870224A CN115870224A CN202310215571.6A CN202310215571A CN115870224A CN 115870224 A CN115870224 A CN 115870224A CN 202310215571 A CN202310215571 A CN 202310215571A CN 115870224 A CN115870224 A CN 115870224A
- Authority
- CN
- China
- Prior art keywords
- collecting box
- belt
- conveying belt
- material collecting
- conveyer belt
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000001514 detection method Methods 0.000 title claims abstract description 43
- 239000000463 material Substances 0.000 claims description 118
- 238000007599 discharging Methods 0.000 claims description 55
- 230000029058 respiratory gaseous exchange Effects 0.000 claims description 31
- 230000000241 respiratory effect Effects 0.000 claims description 28
- 238000009434 installation Methods 0.000 claims description 9
- 238000004891 communication Methods 0.000 claims description 6
- 230000000694 effects Effects 0.000 abstract description 6
- 238000000034 method Methods 0.000 description 15
- 238000012856 packing Methods 0.000 description 7
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 5
- 230000005540 biological transmission Effects 0.000 description 4
- 230000003116 impacting effect Effects 0.000 description 4
- 238000004806 packaging method and process Methods 0.000 description 4
- 238000012545 processing Methods 0.000 description 4
- 230000000903 blocking effect Effects 0.000 description 3
- 238000003825 pressing Methods 0.000 description 3
- 238000004064 recycling Methods 0.000 description 3
- 238000007790 scraping Methods 0.000 description 3
- 230000001360 synchronised effect Effects 0.000 description 3
- 241000588914 Enterobacter Species 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 230000010355 oscillation Effects 0.000 description 1
- 238000011084 recovery Methods 0.000 description 1
- 210000002784 stomach Anatomy 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
Images
Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02W—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO WASTEWATER TREATMENT OR WASTE MANAGEMENT
- Y02W30/00—Technologies for solid waste management
- Y02W30/50—Reuse, recycling or recovery technologies
- Y02W30/62—Plastics recycling; Rubber recycling
Landscapes
- Sorting Of Articles (AREA)
Abstract
The invention discloses a breath card appearance detection system, which comprises a detection body, a main conveying belt and a discharge conveying belt, wherein the main conveying belt and the discharge conveying belt are respectively communicated with a feed inlet and a discharge outlet of the detection body, and the breath card appearance detection system also comprises: the conveying path of the main conveying belt is provided with a converging port, a discharge port of the auxiliary conveying belt is communicated with the converging port, and the conveying direction of the auxiliary conveying belt is perpendicular to the conveying direction of the main conveying belt; the discharge gate of feeding conveyer belt communicates in vice conveyer belt, feeding conveyer belt is on a parallel with main conveyer belt, feeding conveyer belt's feed inlet sets up with the feed inlet syntropy of main conveyer belt. This application has the effect that improves the detection efficiency to the product.
Description
Technical Field
The invention relates to the field of quality detection equipment of a respiratory card, in particular to an appearance detection system of the respiratory card.
Background
With the continuous progress of medical technology, the respiratory card is used for detecting the enterobacter pyloricus in the stomach, so the appearance of the respiratory card needs to be detected before the respiratory card is manufactured, and the quality and the subsequent use effect are improved.
Existing, the machine is examined including the AI vision lamp to the card outward appearance check out test set, feeding conveyer belt and ejection of compact conveyer belt, the feed inlet and the discharge gate that the machine was examined to the AI vision lamp are all on the horizontal direction, feeding conveyer belt and ejection of compact conveyer belt communicate respectively in the feed inlet and the discharge gate that the machine was examined to the AI vision lamp, thereby will wait to detect the card of breathing and get into the feed inlet department of feeding conveyer belt in proper order, can examine the machine with the card of breathing input AI vision lamp, then the staff will detect qualified product from the ejection of compact conveyer belt again and take out the packing.
With respect to the related art in the above, the inventors consider that there is a time difference between the entry of two adjacent products into the feeding conveyor belt, and therefore there is a gap between the two adjacent products conveyed on the feeding conveyor belt, thereby making the detection inefficient.
Disclosure of Invention
In order to improve the detection efficiency of products, the application provides a breath card outward appearance detecting system.
The application provides a respiratory card outward appearance detecting system adopts following technical scheme:
a breath card appearance detection system, comprising: detect body, main conveyer belt and ejection of compact conveyer belt communicate respectively in the feed inlet and the discharge gate that detect the body, still include: the conveying path of the main conveying belt is provided with a converging port, a discharge port of the auxiliary conveying belt is communicated with the converging port, and the conveying direction of the auxiliary conveying belt is perpendicular to the conveying direction of the main conveying belt; the discharge gate of feeding conveyer belt communicates in vice conveyer belt, feeding conveyer belt is on a parallel with main conveyer belt, feeding conveyer belt's feed inlet sets up with the feed inlet syntropy of main conveyer belt.
By adopting the technical scheme, after the respiratory card to be detected is processed from the last processing procedure, the respiratory card to be detected is sequentially placed into the feeding hole of the main conveying belt; meanwhile, the other part of the breath cards to be detected are placed on the feeding conveying belt, and the breath cards to be detected positioned on the feeding conveying belt can be conveyed to the auxiliary conveying belt, so that the orientation of the breath cards to be detected conveyed on the feeding conveying belt is consistent with the orientation of the breath cards to be detected positioned on the main conveying belt, and the breath cards to be detected positioned on the main conveying belt can be conveyed to a position between two adjacent breath cards to be detected positioned on the main conveying belt when conveyed to the position of the junction, so that the time between two adjacent breath cards to be detected conveyed into the detection body is shortened, and the detection efficiency of the breath cards to be detected is improved; in addition, during actual production, after the processing is finished in the previous processing procedure, the next procedure, namely the appearance detection procedure, is carried out from the same side, so that the feeding conveyer belt is required to convey the to-be-detected breath card into the auxiliary conveyer belt, and the use practicability of the system is improved.
Preferably, a mounting frame is installed at the communication position of the feeding conveying belt and the auxiliary conveying belt, a pair of feeding rollers are arranged on the mounting frame at intervals in the vertical direction, and the feeding rollers are rotatably installed on the mounting frame; a gap for the breathing card to pass through is formed between the two feeding rollers, and the two opposite sides of the gap between the two feeding rollers are respectively communicated with the discharge hole of the feeding conveyer belt and the feed hole of the auxiliary conveyer belt; the mounting frame is provided with a first driving piece for driving the feeding roller to rotate; and a first baffle is arranged on one side of the auxiliary conveying belt, which is far away from the feeding conveying belt.
By adopting the technical scheme, because the conveying direction of the feeding conveying belt is different from that of the auxiliary conveying belt, the respiratory card to be detected can be conveyed into the feeding conveying belt only through the feeding conveying belt, so that the respiratory card cannot be fed in the transmission process of the auxiliary conveying belt, and otherwise, the orientation of the respiratory card to be detected can be deviated; after the breath card to be detected is conveyed out of the discharge port of the feeding conveyer belt, the feeding rollers are driven to rotate by the first driving piece, so that the breath card to be detected enters a gap between the two feeding rollers; then the to-be-detected breathing card is quickly conveyed out through the feeding roller and then falls onto the auxiliary conveying belt after impacting the first baffle, and the feeding can be carried out in the transmission process of the auxiliary conveying belt in the process, so that the feeding efficiency is improved.
Preferably, the horizontal height of the gap between the two feeding rollers and the side close to the auxiliary conveying belt is higher than that of the auxiliary conveying belt.
By adopting the technical scheme, the resistance of the breath card to be detected entering the auxiliary conveying belt can be further reduced, and the direction of the breath card to be detected is more accurate when the breath card to be detected is rapidly transmitted out through the feeding roller.
Preferably, a fixed frame is arranged at the communication position of the discharge port and the confluence port of the auxiliary conveyor belt, a pair of buffer conveyor belts are arranged on the fixed frame at intervals in the vertical direction, a gap for a breathing card to pass through is formed between the two buffer conveyor belts, and the two opposite ends of the gap between the two buffer conveyor belts are respectively communicated with the discharge port and the confluence port of the auxiliary conveyor belt; and a second baffle is arranged on one side of the main conveying belt, which is far away from the converging port.
By adopting the technical scheme, because the accuracy needs to be ensured when the breath cards to be detected are converged to the position between two adjacent breath cards to be detected, before the breath cards to be detected on the auxiliary conveying belt enter the main conveying belt, the breath cards to be detected are conveyed into the position between the two cache conveying belts for waiting until the conveying speed of the two cache conveying belts is accelerated when the corresponding convergence port between the two adjacent breath cards to be detected is detected, so that the breath cards to be detected are accelerated to be transmitted out from the position between the two cache conveying belts and fall on the main conveying belt after impacting on the second baffle; the process improves the efficiency and accuracy of conveying the respiratory card to be detected to the position between two adjacent respiratory cards to be detected.
Preferably, the guide rods are arranged right above two sides of the main conveying belt in the conveying direction and are parallel to each other, the same ends of the two guide rods are rotatably arranged on the main conveying belt, and the two guide rods are positioned on one side, away from the feed inlet of the detection body, of the converging inlet; the main conveying belt is provided with a driving assembly for driving the two guide rods to synchronously swing; and a receiving hopper with an opening at the upper part is arranged at one side of the main conveying belt.
Through adopting above-mentioned technical scheme, because after long-time the use, along with the constantly increase of detection error, consequently correspond the condition that the jam appears easily in main conveyer belt convergence entrance position department and entering detection body position department to when the condition of jam appears, start drive assembly orders about two water conservancy diversion poles synchronous oscillation, make two water conservancy diversion poles keep away from rotation department one end and be in directly over the receipts hopper, and then will not carry yet to wait to detect of jam position and breathe the card and lead into in the receipts hopper.
Preferably, the driving assembly includes: the two ends of the linkage rod are respectively hinged to one side of the two guide rods far away from the main conveying belt; the driving cylinder is hinged to the main conveying belt, and a piston rod of the driving cylinder is hinged to the middle position of the linkage rod.
By adopting the technical scheme, the driving cylinder is started, the two guide rods can be synchronously driven to synchronously rotate under the action of the linkage rod, the use of a power source can be reduced, the cost is reduced, and the swing synchronism of the two guide rods can be improved.
Preferably, the method further comprises the following steps: the discharging device comprises a discharging conveyer belt, a plurality of material collecting boxes with openings at the upper parts, a collecting box arranged right below a return section of the discharging conveyer belt and a second driving piece for driving the collecting box to move towards the vertical direction, wherein the discharging conveyer belt is arranged at a discharging opening of the discharging conveyer belt, and the conveying direction of the discharging conveyer belt is perpendicular to the conveying direction of the discharging conveyer belt; a plurality of the material collecting box is arranged along the circumferential direction of the belt body of the discharging conveying belt at intervals, and a limiting mechanism for limiting the breathing card in the material collecting box is arranged at the box opening of the material collecting box.
By adopting the technical scheme, after detection is finished, the qualified respiratory card is output through the discharge hole of the discharge conveyer belt and falls into the corresponding material collecting box, when the single material collecting box is stacked to the capacity of the same packing box during subsequent packing, the discharge conveyer belt is started, and the next material collecting box is moved to the discharge hole of the discharge conveyer belt, so that uninterrupted material collection is achieved, and the collection efficiency is improved; the breathing card is limited in the material collecting box through a limiting mechanism for the fully collected material collecting box; when the collecting box is conveyed to the return section of the discharging conveyer belt and the collecting box fully collected in the return section of the discharging conveyer belt reaches a certain amount, the second driving piece is started to enable the collecting box to vertically move upwards and to be close to the collecting box fully collected in the return section of the discharging conveyer belt, so that after limitation on breathing cards is released through the limiting mechanism, the stacked breathing cards can regularly fall into the collecting box, and when subsequent packaging is carried out, the breathing cards are directly and uniformly packaged in the same packaging box in a stacked mode, and the subsequent packaging efficiency is improved; the process greatly reduces the use of manpower and improves the automation degree.
Preferably, the limiting mechanism comprises: the material collecting box comprises a pair of limiting plates, a pair of torsion springs and a plurality of material pushing plates, wherein mounting holes are formed in two opposite sides of a box opening of the material collecting box, the two limiting plates are rotatably mounted on the material collecting box through the two mounting holes respectively, one end of each limiting plate extends into the material collecting box, and the other end of each limiting plate extends out of the material collecting box; the two torsional springs are respectively sleeved on the rotating shafts of the two limiting plates, one end of each torsional spring is installed on the limiting plate, and the other end of each torsional spring is installed on the material collecting box; stop gear still includes: the locking assembly is used for limiting the vertical orientation position of the limiting plate; the plurality of material pushing plates are arranged in the collecting box at intervals in the conveying direction of the discharging conveying belt, and the plurality of material pushing plates correspond to one end of each limiting plate, which extends out of the material collecting box, one by one.
By adopting the technical scheme, after the fully-collected material collecting box leaves the discharge hole of the discharging conveyer belt, the constraint on the limiting plate is loosened through the locking assembly, the limiting plate drives the limiting plate to rotate under the action of the torsion spring until one end of the limiting plate extends into the material collecting box and the other end extends out of the material collecting box, so that the breathing card can be limited; when starting the second driving piece for the vertical in-process that removes up of collecting box, the effect of accessible scraping wings promotes the limiting plate and extends the outer one end of the case that gathers materials, makes the opening of the case that gathers materials open, accomplishes unloading to the case that gathers materials, and this process is unloaded efficiently, and need not additionally to add the power supply, improves the synchronism.
Preferably, the capture assembly comprises: the side wall of the collecting box provided with the mounting hole is internally provided with a first mounting groove and a second mounting groove which are parallel to each other, the first mounting groove and the second mounting groove are arranged at intervals towards the height direction of the collecting box, the two first mounting grooves are communicated in the mounting hole, and the second mounting groove is communicated with the same side outside the collecting box; the position of the material collecting box between the first mounting groove and the second mounting groove is provided with an inner cavity; the locking block is arranged in the first mounting groove in a sliding manner and extends into the mounting hole, and the elastic piece is arranged at the bottom of the first mounting groove; the push rod is arranged in the second mounting groove in a sliding mode and extends out of the material collecting box; the rotating rod is rotatably arranged in the inner cavity, and two ends of the rotating rod are connected with the locking block and the push rod in a sliding manner respectively; the side wall of one end of the limiting plate, which extends out of the collecting box, is provided with a positioning groove for a locking block to be clamped in, and one side of the locking block, which is far away from one end of the elastic piece and faces the outside of the collecting box, is provided with a guide surface; the frame of the discharge conveyer belt is provided with an actuating piece corresponding to the discharge port and used for pushing the push rod to extend out of one end of the material collecting box.
By adopting the technical scheme, after the fully-collected material collecting box reaches the rack of the discharging conveyer belt and corresponds to the discharging opening, the driving piece is started to push the push rod of the material collecting box to extend out of one end of the material collecting box, so that the constraint of the limiting plate can be loosened, and the breathing card in the material collecting box is limited by the limiting plate; when the limiting plate is pushed to the vertical direction by the material pushing plate, one end, extending out of the material collecting box, of the limiting plate is clamped into the mounting hole, and the locking block is clamped into the positioning groove under the action of the guide surface, so that the limiting plate is locked, and the material is conveniently collected again when the limiting plate is subsequently moved to a discharge hole of the discharge conveyer belt; the structure is simple, and the practicability is high.
Preferably, the urging member includes: the connecting frame is arranged on the frame of the discharging conveyer belt and corresponds to the position of the discharging hole, and the pushing cylinder is arranged on the connecting frame; the starting plate is arranged on a piston rod of the pushing cylinder, and the starting plate is arranged opposite to the two push rods in the same material collecting box.
Through adopting above-mentioned technical scheme, start and promote the cylinder, order about the direction removal of start-up plate towards the push rod, can accomplish and promote the push rod, this simple structure.
In summary, the present application includes at least one of the following beneficial technical effects:
1. when the to-be-detected breath cards positioned on the main conveying belt are conveyed to the position of the junction, the to-be-detected breath cards can be conveyed to the position between two adjacent to-be-detected breath cards positioned on the main conveying belt, so that the time between two adjacent to-be-detected breath cards conveyed into the detection body is shortened, and the detection efficiency of the to-be-detected breath cards is improved;
2. after the breath card to be detected is conveyed out of a discharge port of the feeding conveying belt, the feeding rollers are driven to rotate by the first driving piece, so that the breath card to be detected enters a gap between the two feeding rollers; then the to-be-detected breathing card is quickly conveyed out through the feeding roller and then falls onto the auxiliary conveying belt after impacting on the first baffle, and feeding can be carried out in the transmission process of the auxiliary conveying belt in the process, so that the feeding efficiency is improved;
3. after the breathing card collecting device is used for a long time, along with the continuous increase of detection errors, the blocking situation is easy to occur at the position, corresponding to the converging inlet, of the main conveying belt and the position, corresponding to the position, where the main conveying belt enters the detection body, of the main conveying belt, so that when the blocking situation occurs, the driving assembly is started to drive the two guide rods to synchronously swing, one ends, far away from the rotating positions, of the two guide rods are located right above the material collecting hopper, and then the breathing card to be detected, which is not conveyed to the blocking position, is guided into the material collecting hopper;
4. after the detection is finished, the qualified respiratory card is output through the discharge hole of the discharge conveyer belt and falls into the corresponding material collecting box, when the single material collecting box is stacked to the containing capacity of the same packing box during subsequent packing, the discharge conveyer belt is started, and the next material collecting box is moved to the discharge hole of the discharge conveyer belt, so that uninterrupted material collection is achieved, and the collection efficiency is improved;
5. when starting the second driving piece for the vertical in-process that removes up of collecting box, the effect of accessible scraping wings promotes the limiting plate and extends the outer one end of the case that gathers materials, makes the opening of the case that gathers materials open, accomplishes unloading to the case that gathers materials, and this process is unloaded efficiently, and need not additionally to add the power supply, improves the synchronism.
Drawings
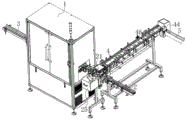
Fig. 1 is a schematic view of the overall structure of embodiment 1 of the present application.
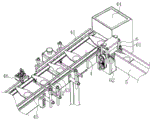
Fig. 2 is a schematic structural view of a joint between the sub-conveyor and the discharge conveyor in embodiment 1 of the present application.
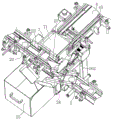
Fig. 3 is a schematic structural view of a joint between a main conveyor belt and an auxiliary conveyor belt in embodiment 1 of the present application.
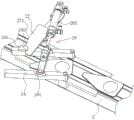
Fig. 4 is a schematic view of a guide pole mounting structure in embodiment 1 of the present application.
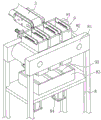
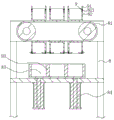
FIG. 5 is a schematic view of the structure of the position of the outfeed conveyor belt of example 2 of the present application.
Fig. 6 is a sectional view of the position between the discharge conveyor belt and the collection box in embodiment 2 of the present application.
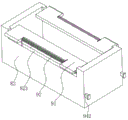
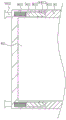
Fig. 7 is a schematic view of the structure of a material collecting box in embodiment 2 of the present application.
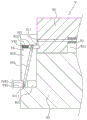
Fig. 8 is a structural sectional view of the capture assembly of embodiment 2 of the present application.
Fig. 9 is a sectional view of a connection structure between a limit plate and a collection box according to embodiment 2 of the present application.
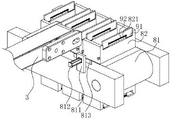
Fig. 10 is a schematic structural view of a discharge conveyor belt in embodiment 2 of the present application.
Description of reference numerals:
1. detecting a body; 2. a main conveyor belt; 21. a sink inlet; 22. a second baffle; 23. pressing a plate; 24. a guide rod; 241. a limiting block; 242. a chute; 25. a material receiving hopper; 26. a drive assembly; 261. a linkage rod; 262. a driving cylinder; 27. a guide plate; 271. a cambered surface; 3. a discharge conveyer belt; 4. a secondary conveyor belt; 41. a first baffle plate; 42. a through hole; 43. a stopper; 44. a recycling bin; 45. a stop bar; 46. positioning the air cylinder; 5. a feeding conveyor belt; 6. a mounting frame; 61. a feeding roller; 62. a first driving member; 7. a fixed mount; 71. caching the conveying belt; 8. a frame body; 81. a discharge conveyer belt; 811. a connecting frame; 812. a push cylinder; 813. a start plate; 82. a material collecting box; 821. mounting holes; 822. a first mounting groove; 823. a second mounting groove; 824. an inner cavity; 83. a collection box; 84. a second driving member; 9. a limiting mechanism; 91. a limiting plate; 911. positioning a groove; 92. a torsion spring; 93. a material pushing plate; 94. a locking assembly; 941. a locking block; 9411. a moving block; 9412. a guide surface; 942. a push rod; 943. an elastic member; 944. rotating the rod; 9441. a yielding groove.
Detailed Description
The present application is described in further detail below with reference to figures 1-10.
The embodiment of the application discloses a breath card appearance detection system.
Example 1
Referring to fig. 1, breathe card outward appearance detecting system including detecting body 1, main conveyer belt 2 and ejection of compact conveyer belt 3, it examines the machine for AI vision lamp to detect body 1, main conveyer belt 2 and the equal level of ejection of compact conveyer belt 3 extend the setting, the discharge gate of main conveyer belt 2 is linked together with the feed inlet that detects body 1, the feed inlet of ejection of compact conveyer belt 3 is linked together with the discharge gate that detects body 1, thereby to wait to detect the breathing card and put into the feed inlet of main conveyer belt 2 in proper order, will wait to detect through main conveyer belt 2 and detect in detecting body 1 breathing card transport, it then carries out from ejection of compact conveyer belt 3 again to detect qualified breathing card.
The appearance detection system of the breath card further comprises an auxiliary conveyor belt 4 and a feeding conveyor belt 5, wherein a converging port 21 is formed in one side of the main conveyor belt 2, which is close to the feeding port of the detection body 1, a discharging port of the auxiliary conveyor belt 4 is communicated with the converging port 21, and the conveying direction of the auxiliary conveyor belt 4 is vertical to the conveying direction of the main conveyor belt 2; the discharge gate of feed conveyor belt 5 communicates in vice conveyer belt 4, and feed conveyor belt 5 is on a parallel with main conveyer belt 2, and the feed inlet of feed conveyor belt 5 sets up with the feed inlet syntropy of main conveyer belt 2 to can put into in the feed inlet department of feed conveyor belt 5 simultaneously and wait to detect the breathing card, through the transport of vice conveyer belt 4 and feed conveyor belt 5, will wait to detect that the breathing card converges to being located main conveyer belt 2 on two adjacent wait to detect the position between the breathing card.
Referring to fig. 1 and 2, an installation frame 6 is fixedly installed at a communication position of a feeding conveyor belt 5 and an auxiliary conveyor belt 4, a pair of feeding rollers 61 is installed in the installation frame 6, the feeding rollers 61 are rubber rollers, the feeding rollers 61 horizontally extend in a direction perpendicular to a conveying direction of the feeding conveyor belt 5, the two feeding rollers 61 are arranged at intervals in a vertical direction, and two ends of each feeding roller 61 are rotatably installed on the installation frame 6; a gap exists between the two feeding rollers 61, two opposite sides of the gap between the two feeding rollers 61 are respectively communicated with the discharge hole of the feeding conveyer belt 5 and the feed hole of the auxiliary conveyer belt 4, and the gap between the two feeding rollers 61 and the discharge hole of the feeding conveyer belt 5 are on the same horizontal straight line, so that the breath card to be detected can enter the gap between the two feeding rollers 61 after being conveyed out of the discharge hole of the feeding conveyer belt 5, and then the breath card to be detected is output from the other side of the gap between the two feeding rollers 61 at an accelerated speed; first driving piece 62 is installed to mounting bracket 6, and first driving piece 62 is the motor, and the output shaft of first driving piece 62 is connected with throwing material roller 61 transmission through the belt drive module to obtain and order about and throw material roller 61 and rotate.
The horizontal height of the gap between the two feeding rollers 61 and the side far away from the feeding conveyer belt 5 is higher than that of the auxiliary conveyer belt 4, so that the resistance of the breath card to be detected in the gap between the two feeding rollers 61 during conveying can be reduced; one side of the auxiliary conveyor belt 4, which is far away from the feeding conveyor belt 5, is fixedly provided with a first baffle plate 41, and a gap between the first baffle plate 41 and the two feeding rollers 61 is arranged oppositely, so that the breathing card to be detected conveyed out in an accelerated manner is blocked and then smoothly falls on the auxiliary conveyor belt 4.
Referring to fig. 2, a through hole 42 is formed in a conveying path of the auxiliary conveying belt 4, a stopper 43 is movably installed in the position, located in the through hole 42, of the auxiliary conveying belt 4 in the vertical direction, an intercepting cylinder is fixedly installed at the bottom of the auxiliary conveying belt 4, and the stopper 43 is fixedly installed on an output shaft of the intercepting cylinder; a recycling box 44 is fixedly arranged at the position of the feeding hole of the auxiliary conveying belt 4, and the recycling box 44 is communicated with the feeding hole of the auxiliary conveying belt 4; therefore, when the front part is blocked, the breath cards to be detected positioned on the auxiliary conveying belt 4 can be intercepted by the stop block 43, then the auxiliary conveying belt 4 is driven to carry out reverse conveying, and the intercepted breath cards to be detected can be sent into the recovery box 44.
The two sides of the auxiliary conveyor belt 4 in the conveying direction are respectively fixedly provided with a stop strip 45, the stop strips 45 extend towards the conveying direction of the auxiliary conveyor belt 4, one side of the auxiliary conveyor belt 4 in the conveying direction is fixedly provided with a positioning cylinder 46, and a piston rod of the positioning cylinder 46 faces the stop strip 45 on the other side of the auxiliary conveyor belt 4 in the conveying direction, so that the positions of the respiratory cards to be detected can be sorted.
Referring to fig. 3, a fixed frame 7 is fixedly installed at a communication position between a discharge port of the auxiliary conveyor belt 4 and the merging port 21, a pair of buffer conveyor belts 71 are installed on the fixed frame 7 at intervals in the vertical direction, the buffer conveyor belts 71 extend in the conveying direction of the auxiliary conveyor belt 4, a gap exists between the two buffer conveyor belts 71, two ends of the gap between the two buffer conveyor belts 71 are respectively communicated with the discharge port of the auxiliary conveyor belt 4 and the merging port 21, and the horizontal height of the gap between the two buffer conveyor belts 71 and one end close to the discharge port of the auxiliary conveyor belt 4 is higher than that of the main conveyor belt 2; therefore, after the respiratory cards to be detected are conveyed out of the discharge port of the auxiliary conveyor belt 4, the respiratory cards to be detected can enter the gap between the two buffer conveyor belts 71 to wait for the position between two adjacent respiratory cards to be detected on the main conveyor belt 2 to move to the corresponding convergence port 21.
A second baffle 22 is fixedly installed on one side, far away from the converging port 21, of the main conveying belt 2, the second baffle 22 is arranged opposite to the converging port 21, so that the breath card to be detected is sent out through the two cache conveying belts 71 in an accelerated manner, and the breath card to be detected stably falls on the main conveying belt 2 after impacting the second baffle 22; the main conveyer belt 2 is fixedly provided with a pressing plate 23 at the position of the junction 21, and the gap between the pressing plate 23 and the main conveyer belt 2 is communicated with the gap between the two buffer conveyer belts 71, so that the situation that the breath card to be detected passes over the second baffle 22 is reduced.
Referring to fig. 3 and 4, the guide rods 24 are respectively installed at positions right above two sides of the main conveying belt 2 in the conveying direction, the two guide rods 24 are arranged in parallel, and the height of a gap between each guide rod 24 and the main conveying belt 2 is smaller than the thickness of the respiratory card to be detected; the two diversion rods 24 are positioned at the side, away from the feed inlet of the detection body 1, of the convergence port 21 in the main conveying belt 2, and one end of each diversion rod 24 is rotatably installed on a frame of the main conveying belt 2; one side fixed mounting that vice conveyer belt 4 was kept away from to main conveyer belt 2 has a receiving hopper 25, and receiving hopper 25 top opening when two guide rods 24 rotate in step to guide rod 24 keep away from the one end of pivot when being in main conveyer belt 2 and keeping away from vice conveyer belt 4 one side, communicate in receiving hopper 25 between two guide rods 24 to can be with waiting to detect the breathing card flow in receiving hopper 25 in main conveyer belt 2.
The main conveying belt 2 is provided with a driving assembly 26 for driving the two guide rods 24 to synchronously swing, the driving assembly 26 comprises a linkage rod 261 and a driving cylinder 262, the linkage rod 261 is positioned between the two guide rods 24, and two ends of the linkage rod 261 are respectively hinged to the middle positions of the two linkage rods 261; drive actuating cylinder 262 and articulate in the main conveyer belt 2 and be close to one side of vice conveyer belt 4, the piston rod that drives actuating cylinder 262 articulates in the intermediate position that the guide bar 24 one side was kept away from to gangbar 261 to can drive two synchronous emergence swings of guide bar 24.
A guide plate 27 is fixedly installed on the main conveying belt 2, the guide plate 27 is horizontally arranged, the guide plate 27 is positioned right above the main conveying belt 2, and a cambered surface 271 extending towards the swing path of the guide rod 24 is arranged on one side, away from the rotating shaft of the guide rod 24, of the guide plate 27; one end fixed mounting that the pivot was kept away from to the water conservancy diversion pole 24 that is located and keeps away from receiving hopper 25 one side has stopper 241, and stopper 241 has been close to pivot one side of water conservancy diversion pole 24 and has been seted up spout 242, and deflector 27 is equipped with one side joint formula of cambered surface 271 and installs in spout 242 to can improve the synchronous swing stability of water conservancy diversion pole 24.
The implementation principle of the embodiment 1 is as follows: after the respiratory card to be detected is processed from the last processing procedure, the respiratory card to be detected is sequentially placed into the feed inlet of the main conveyer belt 2; meanwhile, the other part of the breath cards to be detected are put into the feeding conveyer belt 5, and the breath cards to be detected positioned on the feeding conveyer belt 5 are stably conveyed to the auxiliary conveyer belt 4 through the action of the two feeding rollers 61; when the to-be-detected breath card is conveyed to the position of the corresponding positioning cylinder 46 by the auxiliary conveyor belt 4, the positioning cylinder 46 is started to arrange the to-be-detected breath card; and then stably conveyed into the main conveyor 2 by the action of the two buffer conveyor belts 71.
Example 2
Referring to fig. 5 and 6, the difference between this embodiment and embodiment 1 is that the breath card appearance detecting system further includes a frame body 8, a discharging conveyor belt 81 and a collecting box 82, the discharging conveyor belt 81 is fixedly installed on the frame body 8, the discharging conveyor belt 81 is located at a discharging port of the discharging conveyor belt 3, and the discharging conveyor belt 81 extends horizontally in a direction perpendicular to a conveying direction of the discharging conveyor belt 3; the material collecting boxes 82 are provided with a plurality of material collecting boxes 82, the upper parts of the material collecting boxes 82 are opened, the plurality of material collecting boxes 82 are arranged towards the discharging conveyer belt 81 at intervals, in the embodiment, three material collecting boxes 82 are respectively arranged at the process section and the return section of the discharging conveyer belt 81, and thus the material collecting boxes 82 positioned at the return section of the discharging conveyer belt 81 are opened downwards; therefore, after the detection is finished and the qualified breathing card is output from the discharging conveyer belt 3, the breathing card can fall into the material collecting box 82 for collection; each material collection box 82 is provided with a limiting mechanism 9 for limiting breath cards in the material collection box 82.
The appearance detection system of the breath card further comprises a collecting box 83 and a second driving piece 84, wherein the collecting box 83 is arranged right below the discharging conveyer belt 81, and an opening is formed above the collecting box 83; the second driving member 84 is a cylinder, the second driving member 84 is fixedly mounted on the frame body 8, and a piston rod of the second driving member 84 is fixedly mounted at the bottom of the collecting box 83, so that the collecting box 83 can be driven to move in the vertical direction and be close to the discharging conveyer belt 81.
Referring to fig. 6 and 7, the limiting mechanism 9 includes a pair of limiting plates 91 and a pair of torsion springs 92, a mounting hole 821 is provided at the mouth of each material collecting box 82 and at both ends in the conveying direction of the discharging conveyor belt 81, the two limiting plates 91 are rotatably mounted on the material collecting box 82 through the two mounting holes 821 respectively, the rotating shaft of the limiting plate 91 horizontally extends in the conveying direction perpendicular to the discharging conveyor belt 81, one end of the limiting plate 91 extends into the material collecting box 82, and the other end extends out of the material collecting box 82; the two torsion springs 92 are respectively sleeved on the rotating shafts of the two limiting plates 91, one end of each torsion spring 92 is installed on the limiting plate 91, the other end of each torsion spring 92 is installed on the material collecting box 82, and when the torsion springs 92 are in a natural state, the limiting plates 91 are horizontally arranged, so that the breathing cards stacked in the material collecting box 82 can be limited in the material collecting box 82 when being moved to the return section of the discharging conveying belt 81.
The limiting mechanism 9 further comprises a plurality of material pushing plates 93, the material pushing plates 93 are arranged in a vertical direction, the material pushing plates 93 are arranged in the collecting box 83 at intervals in the conveying direction of the discharging conveying belt 81, the material pushing plates 93 are fixedly mounted at the bottom of the collecting box 83, each material pushing plate 93 is in one-to-one correspondence with one end, extending out of the collecting box 82, of each limiting plate 91 in the three collecting boxes 82 of the discharging conveying belt 81, and therefore when the second driving piece 84 drives the collecting box 83 to vertically move upwards, each collecting box 82 can extend into the position between two adjacent material pushing plates 93 in the collecting box 83, the limiting plates 91 can be pushed to rotate through each material pushing plate 93, and opening of each collecting box 82 is completed.
Referring to fig. 8, a first mounting groove 822 and a second mounting groove 823 are formed in the side wall of the collecting box 82 provided with the mounting hole 821, the first mounting groove 822 and the second mounting groove 823 are arranged at intervals in the height direction of the collecting box 82, the first mounting groove 822 and the second mounting groove 823 are parallel to each other, and the first mounting groove 822 and the second mounting groove 823 horizontally extend along the box wall of the collecting box 82; the two first mounting grooves 822 in the same material collecting box 82 are respectively communicated with the corresponding mounting holes 821, and the two second mounting grooves 823 in the same material collecting box 82 are both communicated with the outside of the same side of the material collecting box 82; inner cavities 824 are formed in the positions, between the first mounting groove 822 and the second mounting groove 823, of the material collecting box 82.
The limiting mechanism 9 further comprises a locking assembly 94 for limiting the vertical orientation position of the limiting plate 91, the locking assembly 94 comprises a locking block 941, a push rod 942, an elastic piece 943 and a rotating rod 944, the locking block 941 is installed on the material collecting box 82 in a sliding mode through the first installation groove 822, one end, far away from the first installation groove 822, of the bottom of the locking block 941 extends into the installation hole 821, a positioning groove 911 is formed in the side wall of one end, extending out of the material collecting box 82, of the limiting plate 91, and one end, extending into the installation hole 821, of the locking block 941 is clamped to the positioning groove 911; the elastic member 943 is a spring, one end of the elastic member 943 is fixedly installed at the bottom of the first installation groove 822, and the other end is fixedly installed at the locking block 941; the push rod 942 is slidably mounted on the material collecting box 82 through the second mounting groove 823, and one end of the push rod 942, which is far away from the second mounting groove 823, extends out of the material collecting box 82; the middle position of the rotating rod 944 is rotatably installed in the inner cavity 824, the two ends of the rotating rod 944 are both provided with a moving groove yielding groove 9441, the yielding groove 9441 extends in the length direction of the rotating rod 944, the locking block 941 and the push rod 942 are both provided with a moving block 9411, and the moving block 9411 of the locking block 941 and the moving block 9411 of the push rod 942 are respectively installed in the two yielding grooves 9441 of the rotating rod 944 in a sliding manner; therefore, when the push rod 942 is pressed to extend out of the end of the material collecting box 82, the locking block 941 can leave the positioning groove 911, and the restriction on the position limiting plate 91 is released.
Referring to fig. 8 and 9, the lock 941 is far away from the one end of elastic component 943 and has seted up the spigot surface 9412 towards the outer one side of collecting box 83 to when the scraping wings 93 promoted the limiting plate 91 and extended the outer one end card of collecting box 82 and go into the mounting hole 821, the effect of accessible spigot surface 9412 makes the lock 941 retract earlier in first mounting groove 822, the elasticity of rethread elastic component 943 is blocked the lock 941 in the constant head tank 911, make the limiting plate 91 stabilize at vertical orientation state.
Referring to fig. 10, an actuating member for pushing a push rod 942 to extend out of one end of the collection box 82 is installed at a position corresponding to the discharge port of the rack of the discharge conveyor belt 81, the actuating member includes a connecting frame 811, a push cylinder 812 and a starting plate 813, the connecting frame 811 is fixedly installed at the discharge port of the discharge conveyor belt 81, and the connecting frame 811 is located at the rack of the discharge conveyor belt 81 and is close to a position of one side of the push rod 942 extending out of the collection box 82; the pushing cylinder 812 is fixedly arranged on the connecting frame 811, and a piston rod of the pushing cylinder 812 extends and retracts towards the sliding direction of the push rod 942; the starting plate 813 is fixedly arranged on a piston rod of the pushing cylinder 812, and the starting plate 813 is arranged opposite to two push rods 942 of the material collecting box 82 at the discharge port of the discharging conveyer belt 81; so that the material collection box 82 rotates the restriction plate 91 to the horizontal position before moving to the return run of the discharge conveyor 81.
The implementation principle of the embodiment 2 is as follows: when the detection is finished, the respiratory card qualified for detection is output through the discharge hole of the discharge conveyer belt 81 and falls into the corresponding material collecting box 82, and when the single material collecting box 82 is stacked to the capacity of the same packing box during subsequent packing, the discharge conveyer belt 81 is started to move the next material collecting box 82 to the discharge hole of the discharge conveyer belt 81; when the fully-collected material collecting box 82 moves to the corresponding starting plate 813, the pushing cylinder 812 is started to push the two pushing rods 942 corresponding to the material collecting box 82, so that the constraint of the limiting plate 91 is released, and the limiting plate 91 is horizontally arranged.
When the three full material collecting boxes 82 reach the return section of the discharging conveyer belt 81, the second driving piece 84 is started to drive the collecting boxes 83 to move towards the direction of the discharging conveyer belt 81, the limiting plates 91 are pushed by the material pushing plates 93 to extend out of one ends of the material collecting boxes 82, the box openings of the material collecting boxes 82 are opened, the breathing cards fall in the collecting boxes 83 to complete collection, and when the breathing cards in the same stack are subsequently packaged, the breathing cards in the same stack are directly packaged in the same packaging box.
The above are preferred embodiments of the present application, and the scope of protection of the present application is not limited thereto, so: all equivalent changes made according to the structure, shape and principle of the present application shall be covered by the protection scope of the present application.
Claims (10)
1. A breath card appearance detection system, comprising: detect body (1), main conveyer belt (2) and ejection of compact conveyer belt (3) communicate respectively in the feed inlet and the discharge gate that detect body (1), its characterized in that still includes: the conveying device comprises an auxiliary conveying belt (4) and a feeding conveying belt (5), wherein a converging port (21) is formed in a conveying path of the main conveying belt (2), a discharging port of the auxiliary conveying belt (4) is communicated with the converging port (21), and the conveying direction of the auxiliary conveying belt (4) is perpendicular to the conveying direction of the main conveying belt (2); the discharge gate of feeding conveyer belt (5) communicates in vice conveyer belt (4), feeding conveyer belt (5) are on a parallel with main conveyer belt (2), the feed inlet of feeding conveyer belt (5) sets up with the feed inlet syntropy of main conveyer belt (2).
2. The appearance detection system for the respiratory card as claimed in claim 1, wherein a mounting frame (6) is installed at a communication position of the feeding conveyor belt (5) and the secondary conveyor belt (4), the mounting frame (6) is provided with a pair of feeding rollers (61) at intervals in a vertical direction, and the feeding rollers (61) are rotatably installed on the mounting frame (6); a gap for the breathing card to pass through is formed between the two feeding rollers (61), and the two opposite sides of the gap between the two feeding rollers (61) are respectively communicated with the discharge hole of the feeding conveyer belt (5) and the feed hole of the auxiliary conveyer belt (4); the mounting frame (6) is provided with a first driving piece (62) for driving the feeding roller (61) to rotate; and a first baffle (41) is arranged on one side of the auxiliary conveying belt (4) far away from the feeding conveying belt (5).
3. The appearance detection system for the respiratory card according to claim 2, wherein the level of the side of the gap between the two feeding rollers (61) close to the secondary conveyor belt (4) is higher than the level of the secondary conveyor belt (4).
4. The appearance detection system for the respiratory card according to claim 1, wherein a fixed frame (7) is installed at a communication position of the discharge port and the confluence port (21) of the auxiliary conveyor belt (4), the fixed frame (7) is provided with a pair of buffer conveyor belts (71) at intervals in the vertical direction, a gap for the respiratory card to pass through is formed between the two buffer conveyor belts (71), and two opposite ends of the gap between the two buffer conveyor belts (71) are respectively communicated with the discharge port and the confluence port (21) of the auxiliary conveyor belt (4); and a second baffle plate (22) is arranged on one side of the main conveying belt (2) far away from the converging port (21).
5. The appearance detection system for the breath card according to claim 1, wherein the main conveyor belt (2) is provided with guide rods (24) directly above two sides in the conveying direction, the guide rods (24) are parallel to each other, the same end of each guide rod (24) is rotatably mounted on the main conveyor belt (2), and the guide rods (24) are located on the side of the collection port (21) far away from the feed port of the detection body (1); the main conveying belt (2) is provided with a driving component (26) for driving the two guide rods (24) to synchronously swing; and a receiving hopper (25) with an opening at the upper part is arranged at one side of the main conveying belt (2).
6. The breath card appearance detection system of claim 5, wherein the drive assembly (26) comprises: the device comprises a linkage rod (261) and a driving cylinder (262), wherein two ends of the linkage rod (261) are respectively hinged to one side, away from the main conveying belt (2), of each guide rod (24); drive actuating cylinder (262) and articulate in main conveyer belt (2), the piston rod that drives actuating cylinder (262) articulates the intermediate position in gangbar (261).
7. The breath card appearance detection system of claim 1, further comprising: the automatic conveying device comprises a discharging conveying belt (81), a plurality of material collecting boxes (82) with openings in the upper portions, a collecting box (83) arranged right below a return section of the discharging conveying belt (81), and a second driving piece (84) used for driving the collecting box (83) to move towards the vertical direction, wherein the discharging conveying belt (81) is arranged at a discharging opening of the discharging conveying belt (3), and the conveying direction of the discharging conveying belt (81) is perpendicular to the conveying direction of the discharging conveying belt (3); a plurality of the material collecting box (82) is arranged along the circumferential direction of the belt body of the discharging conveying belt (81) at intervals, and a limiting mechanism (9) used for limiting the breathing card in the material collecting box (82) is installed at the position of a box opening of the material collecting box (82).
8. The breath card appearance detection system according to claim 7, wherein the position limiting mechanism (9) comprises: the material collecting box comprises a pair of limiting plates (91), a pair of torsion springs (92) and a plurality of material pushing plates (93), wherein mounting holes (821) are formed in two opposite sides of a box opening of the material collecting box (82), the two limiting plates (91) are rotatably mounted on the material collecting box (82) through the two mounting holes (821) respectively, one end of each limiting plate (91) extends into the material collecting box (82), and the other end of each limiting plate extends out of the material collecting box (82); the two torsion springs (92) are respectively sleeved on the rotating shafts of the two limiting plates (91), one end of each torsion spring (92) is installed on each limiting plate (91), and the other end of each torsion spring (92) is installed on the material collecting box (82); the limiting mechanism (9) further comprises: a locking assembly (94) used for limiting the vertical orientation position of the limit plate (91); the plurality of material pushing plates (93) are arranged in the collecting box (83) at intervals in the conveying direction of the discharging conveying belt (81), and the plurality of material pushing plates (93) correspond to one end, extending out of the material collecting box (82), of each limiting plate (91) one by one.
9. The breath card appearance detection system of claim 8, wherein the capture assembly (94) comprises: the material collecting box comprises a locking block (941), a push rod (942), an elastic piece (943) and a rotating rod (944), wherein a first mounting groove (822) and a second mounting groove (823) which are parallel to each other are formed in the side wall of a mounting hole (821) of the material collecting box (82), the first mounting groove (822) and the second mounting groove (823) are arranged towards the height direction of the material collecting box (82) at intervals, the first mounting groove (822) is communicated with the mounting hole (821), and the second mounting groove (823) is communicated with the same side of the material collecting box (82) outside; an inner cavity (824) is formed in the position, located between the first mounting groove (822) and the second mounting groove (823), of the material collecting box (82); the locking block (941) is mounted on the first mounting groove (822) in a sliding mode and extends into the mounting hole (821), and the elastic piece (943) is mounted on the bottom of the first mounting groove (822); the push rod (942) is installed on the second installation groove (823) in a sliding mode and extends out of the material collecting box (82); the rotating rod (944) is rotatably installed in the inner cavity (824), and two ends of the rotating rod (944) are connected with the locking block (941) and the push rod (942) in a sliding manner respectively; a positioning groove (911) for clamping a locking block (941) is formed in the side wall of one end, extending out of the material collecting box (82), of the limiting plate (91), and a guide surface (9412) is arranged on one side, facing out of the collecting box (83), of one end, far away from the elastic piece (943), of the locking block (941); and an actuating piece for pushing the push rod (942) to extend out of one end of the material collecting box (82) is arranged at the position of the rack of the discharging conveying belt (81) and corresponding to the discharging port.
10. The breath card appearance detection system of claim 9, wherein the actuation member comprises: the discharging device comprises a connecting frame (811), a pushing cylinder (812) and a starting plate (813), wherein the connecting frame (811) is installed on the frame of the discharging conveying belt (81) and corresponds to the discharging hole, and the pushing cylinder (812) is installed on the connecting frame (811); the starting plate (813) is arranged on a piston rod of the pushing cylinder (812), and the starting plate (813) is arranged opposite to the two push rods (942) in the same material collecting box (82).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310215571.6A CN115870224B (en) | 2023-03-08 | 2023-03-08 | Respiratory card appearance detection system |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310215571.6A CN115870224B (en) | 2023-03-08 | 2023-03-08 | Respiratory card appearance detection system |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115870224A true CN115870224A (en) | 2023-03-31 |
| CN115870224B CN115870224B (en) | 2023-05-02 |
Family
ID=85762040
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202310215571.6A Active CN115870224B (en) | 2023-03-08 | 2023-03-08 | Respiratory card appearance detection system |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115870224B (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117804687A (en) * | 2023-12-29 | 2024-04-02 | 广州三拓识别技术有限公司 | A continuous hose extrusion leak detection equipment |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1895797A (en) * | 2005-07-11 | 2007-01-17 | S·I精工株式会社 | Agricultural product screening device |
| CN101049595A (en) * | 2007-01-26 | 2007-10-10 | 广州三拓识别技术有限公司 | Extensible inspection production equipment for smart cards |
| JP2018143916A (en) * | 2017-03-01 | 2018-09-20 | 藤本 幸士 | Automatic member inspection system |
| CN109158338A (en) * | 2018-08-02 | 2019-01-08 | 广东六缘智能装备科技有限公司 | A kind of vertical feeding integrated machine for sorting of lithium battery |
| CN209651328U (en) * | 2019-02-18 | 2019-11-19 | 深圳市金鹰鹏物流有限公司 | A kind of multifunctional logistics dispatching handling system |
| WO2020004917A1 (en) * | 2018-06-28 | 2020-01-02 | Cj Logistics Corporation | System and method for controlling spacing between delivery goods on conveyor belt |
| CN112845120A (en) * | 2021-01-14 | 2021-05-28 | 广州市明顿包装制品有限公司 | Visual detection equipment and method for packaging bottle |
| CN113086323A (en) * | 2021-04-07 | 2021-07-09 | 青岛赐来福纺织机械有限公司 | Cheese counter weight mechanism and cheese baling line |
| CN114655661A (en) * | 2022-03-16 | 2022-06-24 | 深圳市恒天伟业科技有限公司 | PCB detection device and detection method |
| CN115593850A (en) * | 2022-11-08 | 2023-01-13 | 东莞市远晟自动化设备有限公司(Cn) | Angle type belt conveyor |
-
2023
- 2023-03-08 CN CN202310215571.6A patent/CN115870224B/en active Active
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1895797A (en) * | 2005-07-11 | 2007-01-17 | S·I精工株式会社 | Agricultural product screening device |
| CN101049595A (en) * | 2007-01-26 | 2007-10-10 | 广州三拓识别技术有限公司 | Extensible inspection production equipment for smart cards |
| JP2018143916A (en) * | 2017-03-01 | 2018-09-20 | 藤本 幸士 | Automatic member inspection system |
| WO2020004917A1 (en) * | 2018-06-28 | 2020-01-02 | Cj Logistics Corporation | System and method for controlling spacing between delivery goods on conveyor belt |
| CN109158338A (en) * | 2018-08-02 | 2019-01-08 | 广东六缘智能装备科技有限公司 | A kind of vertical feeding integrated machine for sorting of lithium battery |
| CN209651328U (en) * | 2019-02-18 | 2019-11-19 | 深圳市金鹰鹏物流有限公司 | A kind of multifunctional logistics dispatching handling system |
| CN112845120A (en) * | 2021-01-14 | 2021-05-28 | 广州市明顿包装制品有限公司 | Visual detection equipment and method for packaging bottle |
| CN113086323A (en) * | 2021-04-07 | 2021-07-09 | 青岛赐来福纺织机械有限公司 | Cheese counter weight mechanism and cheese baling line |
| CN114655661A (en) * | 2022-03-16 | 2022-06-24 | 深圳市恒天伟业科技有限公司 | PCB detection device and detection method |
| CN115593850A (en) * | 2022-11-08 | 2023-01-13 | 东莞市远晟自动化设备有限公司(Cn) | Angle type belt conveyor |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117804687A (en) * | 2023-12-29 | 2024-04-02 | 广州三拓识别技术有限公司 | A continuous hose extrusion leak detection equipment |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115870224B (en) | 2023-05-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4539794A (en) | Automatic machine for unloading and reloading films from and into X ray cassettes | |
| CN105344617B (en) | A kind of blood sample automatic sorting and statistic device | |
| CN206392450U (en) | A roller appearance automatic detection device | |
| CN201002080Y (en) | Nut screening machine | |
| CN113996558B (en) | Finished cigarette disassembling and inspecting device and disassembling and inspecting method thereof | |
| CN108248935A (en) | Axial diode detects automatically, prints and mounted box all-in-one machine | |
| CN115870224B (en) | Respiratory card appearance detection system | |
| CN219519646U (en) | Chip defective sorting mechanism | |
| CN110523642B (en) | Lithium battery sorting type logistics transplanting platform and transplanting method thereof | |
| CN110525715A (en) | A kind of flexible conveying device | |
| CN212216289U (en) | an automatic sorter | |
| CN110999940B (en) | A double-station intestine cutting mechanism and a four-station intestine cutting device | |
| CN111238415B (en) | Automatic detection equipment for valve coaxiality | |
| CN219821854U (en) | Cigarette bar package weighing and pack missing detection device | |
| CN113145471A (en) | Material label screening and detecting device | |
| CN217774865U (en) | A fruit grade grading device | |
| CN218749146U (en) | Automatic detection device for injection molding products | |
| CN207791221U (en) | A kind of supply formula fruit weighing recrater | |
| CN115724009A (en) | A test strip automatic cutting and packaging equipment | |
| CN113998242B (en) | Cigarette packet disassembly and inspection device capable of comprehensively detecting cigarette packets and cigarette appearances | |
| CN216827332U (en) | Novel box support waste kicking machine | |
| CN109351667A (en) | Cell sorting machine | |
| CN114056657B (en) | Full-automatic sausage packaging line | |
| CN223629048U (en) | Tunnel type medicine bag detection machine | |
| CN222872762U (en) | Sausage raw material sorting equipment |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |