CN115739823A - Bottle cap production and assembly process - Google Patents
Bottle cap production and assembly process Download PDFInfo
- Publication number
- CN115739823A CN115739823A CN202211010345.6A CN202211010345A CN115739823A CN 115739823 A CN115739823 A CN 115739823A CN 202211010345 A CN202211010345 A CN 202211010345A CN 115739823 A CN115739823 A CN 115739823A
- Authority
- CN
- China
- Prior art keywords
- bottle cap
- plate
- air
- shell
- assembly process
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images
Landscapes
- Cleaning In General (AREA)
Abstract
本发明提供一种瓶盖生产装配工艺,包括稳定撑架、滤网板、进风壳、导风壳、分流板、延伸随动板、主动皮带轮、第一竖向外螺纹杆以及空气负离子发生器,安装底板上端面安装有带式输送机,第一竖向外螺纹杆环形侧面上侧焊接有主动皮带轮,稳定撑架内侧设置有导风壳,导风壳下端面安装有分流板,导风壳前后端面对称设置有延伸随动板,导风壳上端面焊接有进风壳,进风壳内部上侧插装有滤网板,进风壳内壁左右两侧和前后两侧均对称安装有空气负离子发生器,该设计解决了原有瓶盖除尘方式安全性欠佳的问题,与现有技术相比,本发明结构合理,便于对瓶盖想负离子吹风除尘,并且具备可调能力,适用范围广,可靠性高。

The invention provides a bottle cap production and assembly process, which includes a stable support frame, a filter screen plate, an air inlet shell, an air guide shell, a splitter plate, an extended follower plate, a driving pulley, a first vertical external threaded rod, and an aeronegative ion generator A belt conveyor is installed on the upper surface of the installation base plate, a driving pulley is welded on the upper side of the ring side of the first vertical external threaded rod, an air guide shell is installed on the inner side of the stable support, and a splitter plate is installed on the lower end of the air guide shell. The front and rear ends of the wind shell are symmetrically provided with extended follower plates, the upper end of the air guide shell is welded with an air intake shell, and the upper side of the air intake shell is inserted with a filter plate, and the left and right sides and the front and rear sides of the inner wall of the air intake shell are installed symmetrically There is an air negative ion generator. This design solves the problem of poor safety in the original bottle cap dust removal method. Compared with the existing technology, the present invention has a reasonable structure, which is convenient for blowing and dust removal of negative ions on the bottle cap, and has adjustable capabilities. Wide application range and high reliability.
Description
技术领域technical field
本发明是一种瓶盖生产装配工艺,属于瓶盖生产技术领域。The invention relates to a production and assembly process of a bottle cap, which belongs to the technical field of bottle cap production.
背景技术Background technique
在现有的酒类包装中,玻璃瓶和陶瓷瓶体是最常用的两种瓶体,其瓶盖的密封通常使用塑料密封圈和瓶盖相结合,瓶盖是由多个部件组成。目前,一般采用多个部件分体制作,制作完成后再进行部件组装,进而完成瓶盖的生产。In the existing wine packaging, glass bottles and ceramic bottles are the most commonly used two kinds of bottles, and the sealing of the bottle caps is usually combined with a plastic sealing ring and a bottle cap, and the bottle cap is composed of multiple parts. At present, a plurality of components are generally used for separate production, and after the production is completed, the components are assembled to complete the production of the bottle cap.
由于瓶盖的生产过程较为复杂,生产流水线上需要人力较多,且手工组装效率低,成本较高,并且原有的瓶盖在生产过程中是采用纯净水加洗涤剂进行水洗,而此种清洗方式存在食品安全隐患,现在急需一种瓶盖生产装配工艺解决上述问题。Because the production process of the bottle cap is relatively complicated, more manpower is required on the production line, and the efficiency of manual assembly is low, and the cost is high. In addition, the original bottle cap is washed with pure water and detergent during the production process. There are potential food safety hazards in the cleaning method, and a production and assembly process for bottle caps is urgently needed to solve the above problems.
发明内容Contents of the invention
针对现有技术存在的不足,本发明目的是提供一种瓶盖生产装配工艺,以解决上述背景技术中提出的问题。Aiming at the deficiencies in the prior art, the purpose of the present invention is to provide a production and assembly process for bottle caps to solve the problems raised in the above-mentioned background technology.
为了实现上述目的,本发明是通过如下的技术方案来实现:一种瓶盖生产装配工艺,该生产工艺的具体步骤如下:In order to achieve the above object, the present invention is achieved through the following technical solutions: a production and assembly process for bottle caps, the specific steps of which are as follows:
(1)借助注塑模具对塑料原料进行注塑;(1) Plastic raw materials are injected by means of injection molds;
(2)对注塑成型后的瓶盖进行吹风除尘;(2) Blow and dust the bottle caps after injection molding;
(3)对除尘后的瓶盖表面进行烫印、喷涂、电镀和赋码;(3) Hot stamping, spraying, electroplating and coding on the surface of the bottle cap after dust removal;
(4)对瓶盖进行组立;(4) Assemble the bottle cap;
(5)对瓶盖表面和内部二维码进行关联,并通过外部二维码进行追溯;(5) Associate the surface of the bottle cap with the internal QR code, and trace through the external QR code;
(6)对瓶盖成品与成品瓶身进行组装;(6) Assemble the finished bottle cap and the finished bottle body;
(7)对未被除尘的瓶盖进行测漏,避免未被除尘的瓶盖流入下一道工序;(7) Leak detection is performed on bottle caps that have not been dedusted to prevent the bottle caps that have not been dedusted from flowing into the next process;
(8)对瓶盖外包装箱二维码进行关联,以便通过二维码进行追溯;(8) Associate the QR code of the outer packaging of the bottle cap so that it can be traced through the QR code;
(9)把组装好的瓶盖成品与成品瓶身放入外包装箱中并进行检验,避免破损的外包装箱流入下一道工序;(9) Put the assembled bottle cap and finished bottle body into the outer packaging box and inspect it to prevent the damaged outer packaging box from flowing into the next process;
(10)对外包装箱追溯的数据进行专检;(10) Conduct special inspection on the traceable data of the outer packing box;
(11)把专检后的外包装箱进行入库并借助智能仓库管理系统对产品进行数据交付。(11) Put the specially inspected outer packing boxes into the warehouse and deliver the data of the products with the help of the intelligent warehouse management system.
上述生产工艺中对注塑成型后的瓶盖进行吹风除尘包括:安装底板、稳定撑架、带式输送机、驱动电机、滤网板、进风壳、导风壳、分流板、第二竖向外螺纹杆、延伸随动板、从动皮带轮、风机、主动皮带轮、第一竖向外螺纹杆以及空气负离子发生器,所述安装底板上端面安装有带式输送机,所述安装底板上端面中间位置安装有稳定撑架,所述稳定撑架上端面后侧安装有驱动电机,所述驱动电机下端连接有第一竖向外螺纹杆,所述第一竖向外螺纹杆环形侧面上侧焊接有主动皮带轮,所述稳定撑架内部前侧插装有第二竖向外螺纹杆,所述第二竖向外螺纹杆环形侧面上侧焊接有从动皮带轮,所述稳定撑架内侧设置有导风壳,所述导风壳下端面安装有分流板,所述导风壳前后端面对称设置有延伸随动板,所述导风壳上端面焊接有进风壳,所述进风壳内部上侧插装有滤网板,所述进风壳内部上侧安装有风机,所述进风壳内壁左右两侧和前后两侧均对称安装有空气负离子发生器。In the above production process, blowing and dedusting the injection-molded bottle caps include: installation base plate, stable support frame, belt conveyor, drive motor, filter plate, air inlet shell, air guide shell, splitter plate, second vertical Externally threaded rod, extended follower plate, driven pulley, fan, driving pulley, first vertical externally threaded rod and negative air ion generator, a belt conveyor is installed on the upper surface of the installation base plate, and the upper surface of the installation base plate A stabilizing bracket is installed at the middle position, and a driving motor is installed on the rear side of the upper end surface of the stabilizing bracket. A driving pulley is welded, a second vertical external threaded rod is inserted into the front side of the stabilizing bracket, and a driven pulley is welded on the annular side of the second vertical external threaded rod, and the inner side of the stabilizing bracket is set There is an air guide shell, the lower end of the air guide shell is equipped with a splitter plate, the front and rear end faces of the air guide shell are symmetrically provided with extended follower plates, the upper end of the air guide shell is welded with an air inlet shell, and the air inlet shell A filter plate is inserted on the upper side of the interior, a fan is installed on the upper side of the air intake shell, and negative air ion generators are symmetrically installed on the left and right sides and the front and rear sides of the inner wall of the air intake shell.
进一步地,所述从动皮带轮与主动皮带轮之间缠绕有传动皮带,所述延伸随动板设置有两个,且两个延伸随动板规格相同,所述延伸随动板内部前侧开设有内螺纹竖孔,且内螺纹竖孔分别与第一竖向外螺纹杆和第二竖向外螺纹杆相啮合。Further, a transmission belt is wound between the driven pulley and the driving pulley, there are two extension follower plates, and the specifications of the two extension follower plates are the same, and the front side of the extension follower plate is provided with The internally threaded vertical hole is engaged with the first vertical externally threaded rod and the second vertically externally threaded rod respectively.
进一步地,所述第一竖向外螺纹杆和第二竖向外螺纹杆下端均套装有滚珠轴承,所述稳定撑架内壁前后两侧对称开设有限位凹槽,且限位凹槽与延伸随动板相匹配,所述延伸随动板与导风壳通过焊接方式相连。Further, the lower ends of the first vertical external threaded rod and the second vertical external threaded rod are fitted with ball bearings, and the front and rear sides of the inner wall of the stabilizing bracket are symmetrically provided with limiting grooves, and the limiting grooves and the extension The follower plate is matched, and the extended follower plate is connected with the wind guide shell by welding.
进一步地,所述分流板为可拆装结构,所述分流板内部开设有贯穿孔,且贯穿孔开设有多个,所述滤网板内部右侧穿插有定位销,所述滤网板为可拆装结构,所述滤网板由不织布过滤网制成。Further, the splitter plate is a detachable structure, and there are through holes inside the splitter plate, and there are a plurality of through holes, the right side of the filter screen plate is interspersed with positioning pins, and the filter screen plate is The structure is detachable, and the filter screen plate is made of non-woven filter screen.
进一步地,所述稳定撑架上端面后侧安装有第一堵板,且第一堵板为可拆装结构,所述稳定撑架上端面后侧安装有第二堵板,且第二堵板为可拆装结构,所述空气负离子发生器安装有四个,且四个空气负离子发生器规格相同,所述稳定撑架后端面上侧安装有控制面板,且控制面板输入端通过导线与外界电源相连接,所述风机和四个空气负离子发生器均通过导线与控制面板输出端相连接。Further, a first blocking plate is installed on the rear side of the upper end surface of the stable brace, and the first blocking plate is a detachable structure, and a second blocking plate is installed on the rear side of the upper end surface of the stable brace, and the second blocking plate The plate is a detachable structure, and four negative air ion generators are installed, and the specifications of the four negative air ion generators are the same, and a control panel is installed on the upper side of the rear end surface of the stable support, and the input end of the control panel is connected with the The external power supply is connected, and the blower fan and the four negative air ion generators are all connected with the output terminals of the control panel by wires.
进一步地,所述驱动电机由伺服电机制成,所述驱动电机通过导线与外界伺服电机控制器相连接,所述风机由调速风机制成,所述带式输送机通过导线与外界电源相连接,所述安装底板内部左右两侧对称开设有安装孔。Further, the drive motor is made of a servo motor, the drive motor is connected to the external servo motor controller through a wire, the fan is made of a speed-regulating fan, and the belt conveyor is connected to the external power supply through a wire. Connection, the left and right sides of the inside of the installation bottom plate are symmetrically provided with installation holes.
本发明的有益效果:本发明的一种瓶盖生产装配工艺,因本发明添加了分流板、延伸随动板、风机、主动皮带轮、第一竖向外螺纹杆以及空气负离子发生器,该设计方便对瓶盖进行负离子吹风除尘,解决了原有瓶盖除尘方式安全性欠佳的问题,提高了本发明的除尘安全性。Beneficial effect of the present invention: a kind of bottle cap production assembly process of the present invention, because the present invention has added splitter plate, extension follower plate, blower fan, driving pulley, first vertical external threaded rod and air anion generator, this design It is convenient to perform negative ion blowing and dust removal on the bottle cap, solves the problem of poor safety in the original bottle cap dust removal method, and improves the dust removal safety of the present invention.
附图说明Description of drawings
通过阅读参照以下附图对非限制性实施例所作的详细描述,本发明的其它特征、目的和优点将会变得更明显:Other characteristics, objects and advantages of the present invention will become more apparent by reading the detailed description of non-limiting embodiments made with reference to the following drawings:
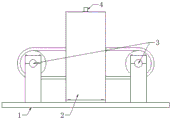
图1为本发明一种瓶盖生产装配工艺中吹风除尘的结构示意图;Fig. 1 is the structural representation of air blowing dust removal in a kind of bottle cap production assembly process of the present invention;
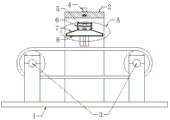
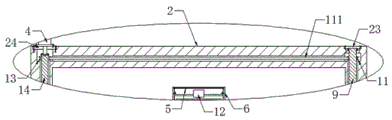
图2为本发明一种瓶盖生产装配工艺中吹风除尘的的正视剖面图;Fig. 2 is the front sectional view of blowing dust removal in a kind of bottle cap production and assembly process of the present invention;
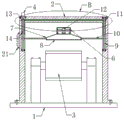
图3为本发明一种瓶盖生产装配工艺中吹风除尘的的左视剖面图;Fig. 3 is a left side sectional view of blowing and dust removal in the production and assembly process of a bottle cap of the present invention;
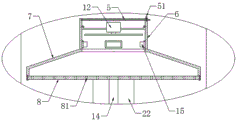
图4为图2中A的放大图;Figure 4 is an enlarged view of A in Figure 2;
图5为图3中B的放大图;Figure 5 is an enlarged view of B in Figure 3;
图6为本发明一种瓶盖生产装配工艺的步骤图;Fig. 6 is a step diagram of a bottle cap production and assembly process of the present invention;
图中: 1-安装底板、2-稳定撑架、21-控制面板、22-限位凹槽、23-第二堵板、24-第一堵板、3-带式输送机、4-驱动电机、5-滤网板、51-定位销、6-进风壳、7-导风壳、8-分流板、81-贯穿孔、9-第二竖向外螺纹杆、10-延伸随动板、11-从动皮带轮、111-传动皮带、12-风机、13-主动皮带轮、14-第一竖向外螺纹杆、15-空气负离子发生器。In the figure: 1-installation base plate, 2-stabilizing bracket, 21-control panel, 22-limiting groove, 23-second blocking plate, 24-first blocking plate, 3-belt conveyor, 4-drive Motor, 5-filter plate, 51-locating pin, 6-inlet shell, 7-wind guide shell, 8-distributor plate, 81-through hole, 9-second vertical external thread rod, 10-extension follower Plate, 11-driven pulley, 111-transmission belt, 12-fan, 13-driving pulley, 14-the first vertical external threaded rod, 15-air anion generator.
具体实施方式Detailed ways
为使本发明实现的技术手段、创作特征、达成目的与功效易于明白了解,下面结合具体实施方式,进一步阐述本发明。In order to make the technical means, creative features, goals and effects achieved by the present invention easy to understand, the present invention will be further described below in conjunction with specific embodiments.
请参阅图1-图6,本发明提供一种技术方案:一种瓶盖生产装配工艺,该生产工艺的具体步骤如下:Please refer to Fig. 1-Fig. 6, the present invention provides a kind of technical solution: a kind of bottle cap production and assembly process, the specific steps of this production process are as follows:
(1)借助注塑模具对塑料原料进行注塑;(1) Plastic raw materials are injected by means of injection molds;
(2)对注塑成型后的瓶盖进行吹风除尘;(2) Blow and dust the bottle caps after injection molding;
(3)对除尘后的瓶盖表面进行烫印、喷涂、电镀和赋码;(3) Hot stamping, spraying, electroplating and coding on the surface of the bottle cap after dust removal;
(4)对瓶盖进行组立;(4) Assemble the bottle cap;
(5)对瓶盖表面和内部二维码进行关联,并通过外部二维码进行追溯;(5) Associate the surface of the bottle cap with the internal QR code, and trace through the external QR code;
(6)对瓶盖成品与成品瓶身进行组装;(6) Assemble the finished bottle cap and the finished bottle body;
(7)对未被除尘的瓶盖进行测漏,避免未被除尘的瓶盖流入下一道工序;(7) Leak detection is performed on bottle caps that have not been dedusted to prevent the bottle caps that have not been dedusted from flowing into the next process;
(8)对瓶盖外包装箱二维码进行关联,以便通过二维码进行追溯;(8) Associate the QR code of the outer packaging of the bottle cap so that it can be traced through the QR code;
(9)把组装好的瓶盖成品与成品瓶身放入外包装箱中并进行检验,避免破损的外包装箱流入下一道工序;(9) Put the assembled bottle cap and finished bottle body into the outer packaging box and inspect it to prevent the damaged outer packaging box from flowing into the next process;
(10)对外包装箱追溯的数据进行专检;(10) Conduct special inspection on the traceable data of the outer packing box;
(11)把专检后的外包装箱进行入库并借助智能仓库管理系统对产品进行数据交付。(11) Put the specially inspected outer packing boxes into the warehouse and deliver the data of the products with the help of the intelligent warehouse management system.
上述生产工艺中对注塑成型后的瓶盖进行吹风除尘包括:安装底板1、稳定撑架2、带式输送机3、驱动电机4、滤网板5、进风壳6、导风壳7、分流板8、第二竖向外螺纹杆9、延伸随动板10、从动皮带轮11、风机12、主动皮带轮13、第一竖向外螺纹杆14以及空气负离子发生器15,安装底板1上端面安装有带式输送机3,安装底板1上端面中间位置安装有稳定撑架2,稳定撑架2上端面后侧安装有驱动电机4,驱动电机4下端连接有第一竖向外螺纹杆14,第一竖向外螺纹杆14环形侧面上侧焊接有主动皮带轮13,稳定撑架2内部前侧插装有第二竖向外螺纹杆9,第二竖向外螺纹杆9环形侧面上侧焊接有从动皮带轮11,稳定撑架2内侧设置有导风壳7,导风壳7下端面安装有分流板8,导风壳7前后端面对称设置有延伸随动板10,导风壳7上端面焊接有进风壳6,进风壳6内部上侧插装有滤网板5,进风壳6内部上侧安装有风机12,进风壳6内壁左右两侧和前后两侧均对称安装有空气负离子发生器15。In the above production process, blowing and dedusting the injection-molded bottle caps include:
从动皮带轮11与主动皮带轮13之间缠绕有传动皮带111,延伸随动板10设置有两个,且两个延伸随动板10规格相同,延伸随动板10内部前侧开设有内螺纹竖孔,且内螺纹竖孔分别与第一竖向外螺纹杆14和第二竖向外螺纹杆9相啮合,传动皮带111方便主动皮带轮13带动从动皮带轮11一同转动,两个延伸随动板10方便带动导风壳7进行升降,而内螺纹竖孔使延伸随动板10具备可上下移动能力,第一竖向外螺纹杆14和第二竖向外螺纹杆9下端均套装有滚珠轴承,稳定撑架2内壁前后两侧对称开设有限位凹槽22,且限位凹槽22与延伸随动板10相匹配,延伸随动板10与导风壳7通过焊接方式相连,滚珠轴承使第一竖向外螺纹杆14和第二竖向外螺纹杆9转动稳定性更好,而限位凹槽22会对延伸随动板10进行限位导向,避免延伸随动板10在上下移动过程中出现偏移或晃动情况。A
分流板8为可拆装结构,分流板8内部开设有贯穿孔81,且贯穿孔81开设有多个,滤网板5内部右侧穿插有定位销51,滤网板5为可拆装结构,滤网板5由不织布过滤网制成,可拆装的分流板8方便后期清洗或更换,多个贯穿孔81方便分流板8对空气进行分流并下侧排出,以便负离子风向下均匀对瓶盖进行除尘,定位销51会对滤网板5进行定位,而由不织布过滤网制成的滤网板5除尘效果更好,避免外部空气中大部分灰尘被一同吸入进风壳6中。The
稳定撑架2上端面后侧安装有第一堵板24,且第一堵板24为可拆装结构,稳定撑架2上端面后侧安装有第二堵板23,且第二堵板23为可拆装结构,空气负离子发生器15安装有四个,且四个空气负离子发生器15规格相同,稳定撑架2后端面上侧安装有控制面板21,且控制面板21输入端通过导线与外界电源相连接,风机12和四个空气负离子发生器15均通过导线与控制面板21输出端相连接,可拆装的第一堵板24方便后期对驱动电机4和第一竖向外螺纹杆14进行拆卸维护,可拆装的第二堵板23方便后期对第二竖向外螺纹杆9进行拆卸维护,四个空气负离子发生器15能够利用高压电晕增加空气中负离子成份,从而改善了空气质量,以便对经过的空气进行除尘降尘,而控制面板21方便工作人员控制风机12和四个空气负离子发生器15工作,驱动电机4由伺服电机制成,驱动电机4通过导线与外界伺服电机控制器相连接,风机12由调速风机12制成,带式输送机3通过导线与外界电源相连接,安装底板1内部左右两侧对称开设有安装孔,由伺服电机制成的驱动电机4方便外界伺服电机控制器控制其转速和力矩,由调速风机12制成的风机12不仅具备可调速能力,同时损耗小、效率高,而安装孔方便对安装底板1进行安装固定。The rear side of the upper end face of the
作为本发明的一个实施例:工作人员首先通过外界伺服电机控制器控制驱动电机4顺时针转动,此时第一竖向外螺纹杆14会带动主动皮带轮13一同转动,而主动皮带轮13会通过传动皮带111带动从动皮带轮11一同转动,进而使从动皮带轮11带动第二竖向外螺纹杆9一同转动,以便第一竖向外螺纹杆14和第二竖向外螺纹杆9同步顺时针转动,此时两组延伸随动板10会带动导风壳7一同向上移动,同理,当控制驱动电机4逆时针转动时,两组延伸随动板10会带动导风壳7一同向下移动,以此对导风壳7使用高度进行调整。As an embodiment of the present invention: the staff first controls the
作为本发明的一个实施例:当导风壳7使用高度调整至所需高度后,工作人员便可以通过控制面板21打开风机12和四个空气负离子发生器15,使风机12通电转动产生抽吸力使进风壳6内部产生负压并把周围空气吸入,在此过程中,滤网板5会对被吸入空气中大部分灰尘进行阻拦,避免外部空气中大部分灰尘被一同吸入进风壳6中,与此同时,四组空气负离子发生器15会通电工作增加空气中负离子成份,从而改善了空气质量,而后负离子空气会被分流板8进行阻挡分流,紧接着多个贯穿孔81会对空气进行分流并下侧排出;然后工作人员便可以启动带式输送机3,而后再把待除尘瓶盖依次搁置在带式输送机3上端面进行输送转移,当瓶盖被输送至分流板8正下方时,排出的负离子空气会对瓶盖表面粘附的进行吹落,以此对瓶盖进行除尘。As an embodiment of the present invention: after the height of the
作为本发明的一个实施例:在后期使用过程中,工作人员只需拔掉定位销51便可以对滤网板5进行拽拉拆卸清洗或更换,当分别对第一堵板24和第二堵板23进行拆卸后,即可分别对驱动电机4和第一竖向外螺纹杆14进行拆卸维护,以及对第二竖向外螺纹杆9进行拆卸维护。As an embodiment of the present invention: in the later use process, the staff only need to pull out the
以上显示和描述了本发明的基本原理和主要特征和本发明的优点,对于本领域技术人员而言,显然本发明不限于上述示范性实施例的细节,而且在不背离本发明的精神或基本特征的情况下,能够以其他的具体形式实现本发明。因此,无论从哪一点来看,均应将实施例看作是示范性的,而且是非限制性的,本发明的范围由所附权利要求而不是上述说明限定,因此旨在将落在权利要求的等同要件的含义和范围内的所有变化囊括在本发明内。The basic principles and main features of the present invention and the advantages of the present invention have been shown and described above. For those skilled in the art, it is obvious that the present invention is not limited to the details of the above-mentioned exemplary embodiments, and without departing from the spirit or fundamentals of the present invention. The present invention can be implemented in other specific forms without any specific features. Accordingly, the embodiments should be regarded in all points of view as exemplary and not restrictive, the scope of the invention being defined by the appended claims rather than the foregoing description, and it is therefore intended that the scope of the invention be defined by the appended claims rather than by the foregoing description. All changes within the meaning and range of equivalents of the elements are embraced in the present invention.
此外,应当理解,虽然本说明书按照实施方式加以描述,但并非每个实施方式仅包含一个独立的技术方案,说明书的这种叙述方式仅仅是为清楚起见,本领域技术人员应当将说明书作为一个整体,各实施例中的技术方案也可以经适当组合,形成本领域技术人员可以理解的其他实施方式。In addition, it should be understood that although this specification is described according to implementation modes, not each implementation mode only contains an independent technical solution, and this description in the specification is only for clarity, and those skilled in the art should take the specification as a whole , the technical solutions in the various embodiments can also be properly combined to form other implementations that can be understood by those skilled in the art.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211010345.6A CN115739823A (en) | 2022-11-29 | 2022-11-29 | Bottle cap production and assembly process |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211010345.6A CN115739823A (en) | 2022-11-29 | 2022-11-29 | Bottle cap production and assembly process |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN115739823A true CN115739823A (en) | 2023-03-07 |
Family
ID=85349334
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202211010345.6A Pending CN115739823A (en) | 2022-11-29 | 2022-11-29 | Bottle cap production and assembly process |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115739823A (en) |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105691883A (en) * | 2016-03-31 | 2016-06-22 | 德阳海普制盖有限公司 | Novel bottle cap with inner and outer double anti-fake codes and manufacturing method of novel bottle cap |
| CN106808725A (en) * | 2017-02-09 | 2017-06-09 | 连云港市金信包装有限公司 | A kind of processing method for identifying bottle cap |
| CN110721961A (en) * | 2019-10-14 | 2020-01-24 | 中航锂电科技有限公司 | Dust removing device |
| CN213468931U (en) * | 2020-09-09 | 2021-06-18 | 东莞市航晨纳米材料有限公司 | Electromagnetic shielding film surface dust removal device |
| CN214078215U (en) * | 2020-11-10 | 2021-08-31 | 青岛澳锐塑料机械有限公司 | Plastic plate production line |
| CN113369161A (en) * | 2021-06-18 | 2021-09-10 | 连云港市金信包装有限公司 | Disc type dust removal detects all-in-one |
| CN215142901U (en) * | 2021-05-25 | 2021-12-14 | 郑州市广源建筑机械制造有限公司 | A dust hood that is easy to install and has good cleanability |
| CN215298256U (en) * | 2021-05-28 | 2021-12-24 | 浙江广厦建设职业技术大学 | Paper archives automatic scanning equipment |
| CN217570535U (en) * | 2022-05-11 | 2022-10-14 | 邓州市瑞泽自动化电子设备有限公司 | Copper strip machine capable of feeding rapidly |
-
2022
- 2022-11-29 CN CN202211010345.6A patent/CN115739823A/en active Pending
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105691883A (en) * | 2016-03-31 | 2016-06-22 | 德阳海普制盖有限公司 | Novel bottle cap with inner and outer double anti-fake codes and manufacturing method of novel bottle cap |
| CN106808725A (en) * | 2017-02-09 | 2017-06-09 | 连云港市金信包装有限公司 | A kind of processing method for identifying bottle cap |
| CN110721961A (en) * | 2019-10-14 | 2020-01-24 | 中航锂电科技有限公司 | Dust removing device |
| CN213468931U (en) * | 2020-09-09 | 2021-06-18 | 东莞市航晨纳米材料有限公司 | Electromagnetic shielding film surface dust removal device |
| CN214078215U (en) * | 2020-11-10 | 2021-08-31 | 青岛澳锐塑料机械有限公司 | Plastic plate production line |
| CN215142901U (en) * | 2021-05-25 | 2021-12-14 | 郑州市广源建筑机械制造有限公司 | A dust hood that is easy to install and has good cleanability |
| CN215298256U (en) * | 2021-05-28 | 2021-12-24 | 浙江广厦建设职业技术大学 | Paper archives automatic scanning equipment |
| CN113369161A (en) * | 2021-06-18 | 2021-09-10 | 连云港市金信包装有限公司 | Disc type dust removal detects all-in-one |
| CN217570535U (en) * | 2022-05-11 | 2022-10-14 | 邓州市瑞泽自动化电子设备有限公司 | Copper strip machine capable of feeding rapidly |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102140753B (en) | Automatic processing flow line of balance ring | |
| CN210253166U (en) | Dust removal and leakage detection integrated machine for bottle cap | |
| CN103872860B (en) | The assembly equipment of micromachine magnet steel | |
| CN208213872U (en) | A kind of parital vacuum type intelligence air purge equipment | |
| CN112467011B (en) | A LED packaging intelligent assembly production line | |
| CN222112397U (en) | Glue filling machine for producing LED nixie tube | |
| CN208758217U (en) | A kind of oscillatory type vial external wall cleaning machine | |
| CN209835030U (en) | Ash removal equipment of chain pipe machine for producing oxidized pellets | |
| CN208663065U (en) | A kind of copper bar machining tool with positioning device | |
| CN105855737A (en) | First assembly device of electric heating rod assembly machine | |
| CN211591760U (en) | Surface printing equipment for textile fabric processing | |
| CN113399347B (en) | A cleaning device for tire production | |
| CN208853364U (en) | A kind of valve cleaning equipment | |
| CN210995033U (en) | Earphone production packaging platform | |
| CN108772374A (en) | A kind of oscillatory type vial external wall cleaning machine | |
| CN209783856U (en) | A leak-proof detection device for a sealed box | |
| CN208341273U (en) | A kind of Novel dry ice cleaning pedestal and its support base group | |
| CN209673302U (en) | A kind of hot nozzle device for detecting sealability | |
| CN116213171A (en) | Spraying equipment and glass production system | |
| CN219923567U (en) | Clean ultraviolet curing tunnel case | |
| CN211669311U (en) | Automatic withstand voltage test machine | |
| CN208715649U (en) | A kind of packaging shrinkage apparatus | |
| CN222178421U (en) | Cooling device for plastic products | |
| CN221819330U (en) | LCD back shell mold | |
| CN207002553U (en) | A kind of infrared ray Anti-explosion bulb production equipment |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20230307 |