CN115722553A - A production and preparation method of 7-series aluminum alloy profiles for automobile lightweight - Google Patents
A production and preparation method of 7-series aluminum alloy profiles for automobile lightweight Download PDFInfo
- Publication number
- CN115722553A CN115722553A CN202211302449.4A CN202211302449A CN115722553A CN 115722553 A CN115722553 A CN 115722553A CN 202211302449 A CN202211302449 A CN 202211302449A CN 115722553 A CN115722553 A CN 115722553A
- Authority
- CN
- China
- Prior art keywords
- fixed
- side wall
- box
- cooling
- aluminum alloy
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images



Landscapes
- Heat Treatments In General, Especially Conveying And Cooling (AREA)
Abstract
Description
技术领域technical field
本发明涉及型材生产技术领域,尤其涉及一种汽车轻量化用7系铝合金型材的生产制备方法。The invention relates to the technical field of profile production, in particular to a method for producing and preparing 7-series aluminum alloy profiles for lightweight vehicles.
背景技术Background technique
随着轻量化要求的越来越高,铝合金型材正向着、薄壁扁宽化、尺寸高精化、形状复杂化和性能高强化方向发展,在新能源汽车上应用的越来越广泛,主要用作电池盒、防撞梁、座椅支架等;With the increasingly high requirements for lightweight, aluminum alloy profiles are developing in the direction of thinner walls, flatter widths, high precision dimensions, complex shapes, and high performance enhancements. They are more and more widely used in new energy vehicles. Used as battery box, anti-collision beam, seat bracket, etc.;
现有的,一般的铝型材生产过程中加热淬火冷却一般为采用液浸式,这种冷却方法对铝型材的冷却不均匀,使铝型材的表面各处刚度分布不均匀,并且整体需要等待较长时间,热量散发速度较慢,整体效率较低。Existing, the heating, quenching and cooling in the production process of general aluminum profiles generally adopt liquid immersion type. This cooling method does not cool the aluminum profiles uniformly, so that the stiffness distribution of the surface of the aluminum profiles is uneven, and the whole needs to wait for a longer period of time. Over a long period of time, the heat dissipation rate is slower and the overall efficiency is lower.
发明内容Contents of the invention
本发明的目的是为了解决现有技术中效率低效果差的问题,而提出的一种汽车轻量化用7系铝合金型材的生产制备方法。The purpose of the present invention is to solve the problem of low efficiency and poor effect in the prior art, and propose a production and preparation method of 7 series aluminum alloy profiles for automobile lightweight.
为了实现上述目的,本发明采用了如下技术方案:一种汽车轻量化用7系铝合金型材的生产制备方法,包括以下步骤:In order to achieve the above object, the present invention adopts the following technical scheme: a production and preparation method of 7-series aluminum alloy profiles for lightweight automobiles, comprising the following steps:
步骤一:高强7系铝合金挤压型材模具优化设计,提升模具通过量,降低单位模具成本;Step 1: Optimize the design of high-strength 7-series aluminum alloy extrusion profile molds, increase the throughput of the mold, and reduce the unit mold cost;
步骤二:铸锭梯度加热实现等温挤压,提升生产效率;Step 2: Gradient heating of the ingot to achieve isothermal extrusion and improve production efficiency;
步骤三:在线淬火工艺及装置;Step 3: On-line quenching process and device;
步骤四:在线整形装置,保证型材的直线度、平面度及垂直度,提升产品成品率;Step 4: Online shaping device to ensure the straightness, flatness and verticality of the profile, and improve the product yield;
上述汽车轻量化用7系铝合金型材的生产制备方法中使用到的设备包括处理箱,所述处理箱的上端安装有盖板,所述处理箱的下部开设有冷却腔,所述冷却腔的内部安装有水泵,所述处理箱的侧壁开设有供水腔,所述水泵出水管与供水腔接通,所述供水腔的侧壁安装有多组喷头,所述处理箱的侧壁开设有排出槽,所述处理箱的内壁固定有回转电机,所述回转电机的输出轴固定有夹持台,所述夹持台的内部设有夹持机构,所述处理箱的内壁转动连接有回转框,所述回转框的内壁固定有缠绕电机,所述缠绕电机的输出轴固定有绞合台,所述绞合台的内部设有绞紧机构,所述夹持机构和绞紧机构共同连接有一对搭载板,所述搭载板的侧壁开设有多个通槽,所述搭载板的侧壁固定有限位板。The equipment used in the production and preparation method of the above-mentioned 7-series aluminum alloy profiles for lightweight automobiles includes a treatment box, a cover plate is installed on the upper end of the treatment box, and a cooling chamber is opened at the bottom of the treatment box. A water pump is installed inside, a water supply chamber is provided on the side wall of the treatment box, and the outlet pipe of the water pump is connected to the water supply chamber, and multiple groups of nozzles are installed on the side wall of the water supply chamber, and a water supply chamber is provided on the side wall of the treatment box. A discharge slot, the inner wall of the processing box is fixed with a rotary motor, the output shaft of the rotary motor is fixed with a clamping platform, the inside of the clamping platform is provided with a clamping mechanism, and the inner wall of the processing box is rotatably connected with a rotary frame, the inner wall of the revolving frame is fixed with a winding motor, the output shaft of the winding motor is fixed with a twisting platform, the inside of the twisting platform is provided with a tightening mechanism, and the clamping mechanism and the tightening mechanism are connected together There is a pair of carrying plates, the side walls of the carrying plates are provided with a plurality of through grooves, and the side walls of the carrying plates are fixed with a limiting plate.
在上述的加工设备中,所述夹持机构包括连接块,所述连接块的两侧均固定有丝杆,所述夹持台的侧壁对称固定有夹持电机和配重块,其中一个所述丝杆与夹持电机的输出轴相固定,另一个所述丝杆与配重块端部转动连接,两个所述丝杆的侧壁均贯穿螺纹连接有滑块,所述滑块与对应搭载板相固定。In the above-mentioned processing equipment, the clamping mechanism includes a connecting block, screw rods are fixed on both sides of the connecting block, and a clamping motor and a counterweight are symmetrically fixed on the side wall of the clamping table, one of which The screw rod is fixed to the output shaft of the clamping motor, the other screw rod is connected to the end of the counterweight in rotation, and the side walls of the two screw rods are threaded and connected with sliders, and the sliders Fixed with the corresponding mounting plate.
在上述的加工设备中,所述夹持台的内部开设有滚槽,所述滚槽的侧壁贯穿开设有滑槽,所述滑块的侧壁转动连接有转杆,所述转杆贯穿滑槽并固定有齿轮,所述滚槽的内壁固定有齿条,所述齿条与齿轮相啮合。In the above-mentioned processing equipment, a rolling groove is provided inside the clamping table, and a chute is opened through the side wall of the rolling groove, and a rotating rod is connected to the side wall of the slider in rotation, and the rotating rod runs through The chute is also fixed with a gear, and the inner wall of the rolling groove is fixed with a rack, and the rack is meshed with the gear.
在上述的加工设备中,所述绞紧机构包括固定于缠绕电机输出轴的缠绕轴,所述绞合台的内壁滑动连接有一对连接板,所述连接板的侧壁固定有挂耳,所述挂耳与缠绕轴共同连接有锁链,所述绞合台的侧壁固定有贯穿连接板的导向杆,所述连接板与搭载板的侧壁相固定。In the above processing equipment, the twisting mechanism includes a winding shaft fixed to the output shaft of the winding motor, a pair of connecting plates are slidably connected to the inner wall of the twisting table, and hanging lugs are fixed on the side walls of the connecting plates. The hanging lug and the winding shaft are jointly connected with a chain, and the side wall of the twisting platform is fixed with a guide rod passing through the connecting plate, and the connecting plate is fixed with the side wall of the carrying plate.
在上述的加工设备中,所述处理箱的侧壁固定有回收箱,所述回收箱的内壁固定有气泵,所述气泵的进气口连接有抽气管,所述抽气管与盖板内部接通,所述盖板的底部安装有多个抽气头。In the above-mentioned processing equipment, the side wall of the treatment box is fixed with a recovery box, the inner wall of the recovery box is fixed with an air pump, the air inlet of the air pump is connected with a suction pipe, and the suction pipe is connected to the inside of the cover plate. Through, the bottom of the cover plate is installed with a plurality of suction heads.
在上述的加工设备中,所述处理箱的侧壁固定有降温箱,所述排出槽与降温箱内部接通,所述降温箱的侧壁插设有与冷却腔接通的回流管,所述回收箱的侧壁固定有气流箱,所述回收箱的侧壁贯穿插设有多个散热片。In the above-mentioned processing equipment, a cooling box is fixed on the side wall of the treatment box, the discharge groove is connected to the inside of the cooling box, and a return pipe connected to the cooling chamber is inserted in the side wall of the cooling box, so An airflow box is fixed on the side wall of the recovery box, and a plurality of cooling fins are inserted through the side wall of the recovery box.
在上述的加工设备中,所述处理箱的外壁固定有涡流管,所述涡流管的冷气流管连接有速冷管和气流管,所述降温箱的侧壁贯穿插设有多个与速冷管接通的接触管,所述气流管与气流箱内部接通,所述气流箱的侧壁贯穿开设有排出口,所述气流管内径小于速冷管内径。In the above-mentioned processing equipment, the outer wall of the treatment box is fixed with a vortex tube, the cold flow tube of the vortex tube is connected with a quick cooling tube and a flow tube, and the side wall of the cooling box is inserted with a plurality of The contact pipe connected to the cold pipe, the airflow pipe is connected to the inside of the airflow box, the side wall of the airflow box is penetrated with a discharge port, and the inner diameter of the airflow pipe is smaller than the inner diameter of the quick cooling pipe.
与现有的技术相比,本发明的优点在于:Compared with the prior art, the present invention has the advantages of:
1、本发明中,持电机工作,使得两个搭载板能够将中间的型材夹紧,两侧同时进行移动,能够实现快速对等的夹持,从而提高夹持效果和效率;1. In the present invention, the holding motor works, so that the two carrying plates can clamp the profile in the middle, and both sides move at the same time, which can realize fast equal clamping, thereby improving the clamping effect and efficiency;
2、本发明中,滑块直接横移受到齿的限制,故而保证滑块位置的稳定性,从而提高夹持效果,并且降低了锁紧后丝杆表面螺纹的损伤,使得丝杆的使用寿命得到提升;2. In the present invention, the direct lateral movement of the slider is limited by the teeth, thus ensuring the stability of the position of the slider, thereby improving the clamping effect, and reducing the damage to the thread on the surface of the screw rod after locking, so that the service life of the screw rod be promoted;
3、本发明中,两个连接板受到拉力而存在相互靠近趋势,进而使得两个搭载板进一步受力从而提高夹紧效果,并且两侧分别作用,可面对较长的型材的处理;3. In the present invention, the two connecting plates have a tendency to approach each other under the tension, so that the two carrying plates are further stressed to improve the clamping effect, and the two sides act separately, which can face the processing of longer profiles;
4、本发明中,通过水泵向供水腔内部通入冷却液进而使得冷却液从喷头喷出,进而通过多面覆盖实现对回转中的型材的高效淬火处理,并且回转加工能够提高均匀程度,提高淬火质量;4. In the present invention, the cooling liquid is passed into the water supply chamber through the water pump, and then the cooling liquid is sprayed from the nozzle, and the high-efficiency quenching treatment of the rotating profile is realized by covering multiple surfaces, and the rotary processing can improve the uniformity and improve the quenching process. quality;
5、本发明中,通过速冷管向接触管通气低温气流,使得处理箱内部的冷却液通过排出槽进入到降温箱后,能够得到低温气流的有效降温处理,从而再由回流管回到冷却腔中,使得冷却液能够在时间相对长的加工中得到高效的循环利用。5. In the present invention, the low-temperature airflow is ventilated to the contact pipe through the quick-cooling pipe, so that the cooling liquid inside the processing box enters the cooling box through the discharge tank, and the effective cooling treatment of the low-temperature airflow can be obtained, thereby returning to the cooling chamber through the return pipe. In the cavity, the coolant can be efficiently recycled in relatively long processing.
附图说明Description of drawings
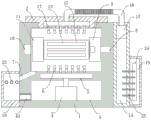
图1为本发明提出的一种汽车轻量化用7系铝合金型材的生产制备方法的结构示意图;Fig. 1 is the structural representation of the production preparation method of a kind of automobile light weight that proposes with 7 series aluminum alloy profiles in the present invention;
图2为本发明提出的一种汽车轻量化用7系铝合金型材的生产制备方法的半剖视图;Fig. 2 is a semi-sectional view of a production and preparation method of a 7-series aluminum alloy profile for automobile lightweight proposed by the present invention;
图3为本发明提出的一种汽车轻量化用7系铝合金型材的生产制备方法的俯剖视图;Fig. 3 is a top sectional view of a production and preparation method of a 7-series aluminum alloy profile for automobile lightweight proposed by the present invention;
图4为本发明提出的一种汽车轻量化用7系铝合金型材的生产制备方法的夹持台部分的结构示意图;Fig. 4 is a schematic structural view of the clamping table part of the production and preparation method of a 7-series aluminum alloy section bar for automobile lightweight proposed by the present invention;
图5为本发明提出的一种汽车轻量化用7系铝合金型材的生产制备方法的绞合台部分的结构示意图。Fig. 5 is a structural schematic diagram of the stranding table part of a method for producing and preparing 7-series aluminum alloy profiles for lightweight automobiles proposed by the present invention.
图中:1处理箱、2盖板、3冷却腔、4水泵、5供水腔、6喷头、7排出槽、8回转电机、9夹持台、10回转框、11绞合台、12搭载板、13通槽、14回收箱、15气泵、16抽气管、17抽气头、18降温箱、19气流箱、20涡流管、21速冷管、22气流管、23接触管、24排出口、25散热片、26夹持电机、27配重块、28丝杆、29连接块、30滑块、31滑槽、32滚槽、33转杆、34齿轮、35齿条、36缠绕电机、37缠绕轴、38连接板、39挂耳、40锁链、41导向杆、42限位板、43回流管。In the figure: 1 treatment box, 2 cover plate, 3 cooling chamber, 4 water pump, 5 water supply chamber, 6 nozzle, 7 discharge tank, 8 rotary motor, 9 clamping table, 10 rotary frame, 11 stranding table, 12 carrying plate , 13 through tank, 14 recovery box, 15 air pump, 16 suction pipe, 17 suction head, 18 cooling box, 19 airflow box, 20 vortex tube, 21 speed cooling pipe, 22 airflow pipe, 23 contact pipe, 24 outlet, 25 heat sink, 26 clamping motor, 27 counterweight, 28 screw rod, 29 connecting block, 30 slider, 31 chute, 32 rolling groove, 33 rotating rod, 34 gear, 35 rack, 36 winding motor, 37 Winding shaft, 38 connecting plate, 39 hanging lug, 40 chain, 41 guide rod, 42 limit plate, 43 return pipe.
具体实施方式Detailed ways
以下实施例仅处于说明性目的,而不是想要限制本发明的范围。The following examples are for illustrative purposes only and are not intended to limit the scope of the invention.
实施例Example
参照图1-5,一种汽车轻量化用7系铝合金型材的生产制备方法,包括以下步骤:Referring to Figures 1-5, a method for producing and preparing 7-series aluminum alloy profiles for lightweight vehicles comprises the following steps:
步骤一:高强7系铝合金挤压型材模具优化设计,提升模具通过量,降低单位模具成本;模具通过量由原来的2吨提升为4吨,单位模具成本降低50%;Step 1: Optimize the design of the high-strength 7-series aluminum alloy extrusion profile mold, increase the throughput of the mold, and reduce the unit mold cost; the mold throughput is increased from the original 2 tons to 4 tons, and the unit mold cost is reduced by 50%;
步骤二:铸锭梯度加热实现等温挤压,提升生产效率;出料温度和型材组织性能均匀稳定;Step 2: Gradient heating of the ingot to achieve isothermal extrusion and improve production efficiency; the discharge temperature and profile structure are uniform and stable;
步骤三:在线淬火工艺及装置Step 3: On-line quenching process and device
步骤四:在线整形装置,保证型材的直线度、平面度及垂直度,提升产品成品率;出料温度和型材组织性能均匀稳定,生产效率高;Step 4: The online shaping device ensures the straightness, flatness and verticality of the profile, and improves the product yield; the output temperature and profile structure are uniform and stable, and the production efficiency is high;
上述汽车轻量化用7系铝合金型材的生产制备方法中使用到的设备包括处理箱1,处理箱1的上端安装有盖板2,处理箱1的下部开设有冷却腔3,冷却腔3的内部安装有水泵4,处理箱1的侧壁开设有供水腔5,水泵4出水管与供水腔5接通,供水腔5的侧壁安装有多组喷头6,处理箱1的侧壁开设有排出槽7,处理箱1的内壁固定有回转电机8,回转电机8的输出轴固定有夹持台9,夹持台9的内部设有夹持机构,处理箱1的内壁转动连接有回转框10,回转框10的内壁固定有缠绕电机36,缠绕电机36的输出轴固定有绞合台11,绞合台11的内部设有绞紧机构,夹持机构和绞紧机构共同连接有一对搭载板12,搭载板12的侧壁开设有多个通槽13,搭载板12的侧壁固定有限位板42。The equipment used in the production and preparation method of the above-mentioned 7-series aluminum alloy profiles for lightweight automobiles includes a
夹持机构包括连接块29,连接块29的两侧均固定有丝杆28,夹持台9的侧壁对称固定有夹持电机26和配重块27,其中一个丝杆28与夹持电机26的输出轴相固定,另一个丝杆28与配重块27端部转动连接,两个丝杆28的侧壁均贯穿螺纹连接有滑块30,滑块30与对应搭载板12相固定。Clamping mechanism comprises connecting
夹持台9的内部开设有滚槽32,滚槽32的侧壁贯穿开设有滑槽31,滑块30的侧壁转动连接有转杆33,转杆33贯穿滑槽31并固定有齿轮34,滚槽32的内壁固定有齿条35,齿条35与齿轮34相啮合,利用齿的啮合实现对横向移动的限位,提高夹持稳定性,降低夹持作用力对丝杆28螺纹的损伤。The inside of the clamping table 9 is provided with a
绞紧机构包括固定于缠绕电机36输出轴的缠绕轴37,绞合台11的内壁滑动连接有一对连接板38,连接板38的侧壁固定有挂耳39,挂耳39与缠绕轴37共同连接有锁链40,绞合台11的侧壁固定有贯穿连接板38的导向杆41,连接板38与搭载板12的侧壁相固定,利用缠绕轴37卷收锁链40,从而提高对型材的夹持效果。The twisting mechanism includes a
处理箱1的侧壁固定有回收箱14,回收箱14的内壁固定有气泵15,气泵15的进气口连接有抽气管16,抽气管16与盖板2内部接通,盖板2的底部安装有多个抽气头17,利用气泵15实现对气化后的冷却液排出,避免冷却液液化回流影响淬火质量。The side wall of the
处理箱1的侧壁固定有降温箱18,排出槽7与降温箱18内部接通,降温箱18的侧壁插设有与冷却腔3接通的回流管43,回收箱14的侧壁固定有气流箱19,回收箱14的侧壁贯穿插设有多个散热片25,利用散热片25进行导热,再经过气流流动带走热量,实现持续的降温处理。The side wall of the
处理箱1的外壁固定有涡流管20,涡流管20的冷气流管连接有速冷管21和气流管22,降温箱18的侧壁贯穿插设有多个与速冷管21接通的接触管23,气流管22与气流箱19内部接通,气流箱19的侧壁贯穿开设有排出口24,气流管22内径小于速冷管21内径,涡流管20与外部空压机连接后,可供应冷气流,从而使得对速冷管21由大批量的冷气流转移,用于快速的降温,使得冷却液能够快速进入循环,而少部分冷气流供应至气流管22,从而对气化后的冷却液进行较为缓慢的持续散热处理;The outer wall of the
本发明中,在实际处理时,将待淬火的型材夹持放置在两个搭载板12中间,然后启动夹持电机26,使其带动丝杆28转动,两个丝杆28转动将同时驱动两个滑块30移动,并且由于螺纹旋向相反,故而两个滑块30将会相向运动,进而使得两个限位板42靠近,随后在型材未夹紧前,撤去型材搬运部件,然后夹持电机26继续工作,使得两个搭载板12能够将中间的型材夹紧,两侧同时进行移动,能够实现快速对等的夹持,从而提高夹持效果和效率;In the present invention, during actual processing, the profile to be quenched is clamped and placed in the middle of the two carrying
在滑块30运动的过程中,转杆33随之移动,转杆33上的齿轮34也将移动,从而使得齿轮34沿着齿条35滚动前进,在后续夹持结束时,齿条35对齿轮34起到移动限位作用,使得滑块30直接横移受到齿的限制,故而保证滑块30位置的稳定性,从而提高夹持效果,并且降低了锁紧后丝杆28表面螺纹的损伤,使得丝杆28的使用寿命得到提升;During the movement of the slider 30, the rotating rod 33 moves thereupon, and the
随后启动缠绕电机36,使其带动缠绕轴37转动,通过缠绕轴37回转有效的缠绕锁链40,进而使得两个连接板38受到拉力而存在相互靠近趋势,进而使得两个搭载板12进一步受力从而提高夹紧效果,并且两侧分别作用,可面对较长的型材的处理;Then start the winding
夹持结束后,可启动回转电机8,通过回转电机8驱动被夹持的型材回转,并且启动水泵4,通过水泵4向供水腔5内部通入冷却液进而使得冷却液从喷头6喷出,进而通过多面覆盖实现对回转中的型材的高效淬火处理,并且回转加工能够提高均匀程度,提高淬火质量;After the clamping is completed, the
同时启动气泵15,气泵15通过抽气管16及抽气头17抽取处理箱1上部气流,从而使得气化的冷却液能够快速的外排,从而避免回落降低淬火质量,而气化的冷却液则进入到回收箱14中,进而冷凝收集,从而循环使用;Simultaneously start the
并且涡流管20也将启动,进而通过速冷管21向接触管23通气低温气流,使得处理箱1内部的冷却液通过排出槽7进入到降温箱18后,能够得到低温气流的有效降温处理,从而再由回流管43回到冷却腔3中,使得冷却液能够在时间相对长的加工中得到高效的循环利用;And the
而小部分低温气流通过气流管22注入到气流箱19中,提高气流箱19内部气流的流动速度,并且时低温气流,使得散热片25能够更好的将回收箱14内部热量导出,进而使得回收箱14内部回收的冷却液得到持续的降温处理,从而便于后续更好的回收利用。And a small part of the low-temperature airflow is injected into the
以上所述仅为本发明的较佳实施例,并不用以限制本发明,凡在本发明的精神和原则之内,所作的任何修改、等同替换、改进等,均应包含在本发明的保护范围之内。The above descriptions are only preferred embodiments of the present invention, and are not intended to limit the present invention. Any modifications, equivalent replacements, improvements, etc. made within the spirit and principles of the present invention shall be included in the protection of the present invention. within range.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211302449.4A CN115722553A (en) | 2022-10-24 | 2022-10-24 | A production and preparation method of 7-series aluminum alloy profiles for automobile lightweight |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211302449.4A CN115722553A (en) | 2022-10-24 | 2022-10-24 | A production and preparation method of 7-series aluminum alloy profiles for automobile lightweight |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN115722553A true CN115722553A (en) | 2023-03-03 |
Family
ID=85293799
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202211302449.4A Pending CN115722553A (en) | 2022-10-24 | 2022-10-24 | A production and preparation method of 7-series aluminum alloy profiles for automobile lightweight |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115722553A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117463889A (en) * | 2023-11-03 | 2024-01-30 | 仪征常众汽车部件有限公司 | An automobile hardware processing and pressing device and its use method |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1425398A (en) * | 1964-12-04 | 1966-01-24 | Creusot Forges Ateliers | Water mist quenching installation, for heavy revolving parts in horizontal position |
| CN202359162U (en) * | 2011-11-18 | 2012-08-01 | 姚强 | Quench machining tool for axle tube |
| CN108772834A (en) * | 2018-08-03 | 2018-11-09 | 山东省科学院海洋仪器仪表研究所 | A kind of Multi-freedom-degreemanipulator manipulator |
| CN208758354U (en) * | 2018-10-01 | 2019-04-19 | 佛山市新义昌金属制品有限公司 | A kind of stainless steel thickness square tube molding machine |
| CN110983009A (en) * | 2019-12-02 | 2020-04-10 | 江苏伯能机床制造有限公司 | Heat treatment device for producing rotary shaft of machine tool |
| CN112171342A (en) * | 2020-10-13 | 2021-01-05 | 杭州云勃机械设计有限公司 | Left-right rotation screw rod translation type clamp holder and using method thereof |
| CN212688134U (en) * | 2020-06-24 | 2021-03-12 | 德清县杰创机械有限公司 | A quenching device for copper and horse processing |
| CN214979440U (en) * | 2021-07-22 | 2021-12-03 | 山东威格特数控科技有限公司 | High-efficient safe numerical control processing equipment |
-
2022
- 2022-10-24 CN CN202211302449.4A patent/CN115722553A/en active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1425398A (en) * | 1964-12-04 | 1966-01-24 | Creusot Forges Ateliers | Water mist quenching installation, for heavy revolving parts in horizontal position |
| CN202359162U (en) * | 2011-11-18 | 2012-08-01 | 姚强 | Quench machining tool for axle tube |
| CN108772834A (en) * | 2018-08-03 | 2018-11-09 | 山东省科学院海洋仪器仪表研究所 | A kind of Multi-freedom-degreemanipulator manipulator |
| CN208758354U (en) * | 2018-10-01 | 2019-04-19 | 佛山市新义昌金属制品有限公司 | A kind of stainless steel thickness square tube molding machine |
| CN110983009A (en) * | 2019-12-02 | 2020-04-10 | 江苏伯能机床制造有限公司 | Heat treatment device for producing rotary shaft of machine tool |
| CN212688134U (en) * | 2020-06-24 | 2021-03-12 | 德清县杰创机械有限公司 | A quenching device for copper and horse processing |
| CN112171342A (en) * | 2020-10-13 | 2021-01-05 | 杭州云勃机械设计有限公司 | Left-right rotation screw rod translation type clamp holder and using method thereof |
| CN214979440U (en) * | 2021-07-22 | 2021-12-03 | 山东威格特数控科技有限公司 | High-efficient safe numerical control processing equipment |
Non-Patent Citations (1)
| Title |
|---|
| 上海市热处理协会等: "实用热处理手册", vol. 2, 30 April 2014, 上海科学技术出版社, pages: 640 - 642 * |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117463889A (en) * | 2023-11-03 | 2024-01-30 | 仪征常众汽车部件有限公司 | An automobile hardware processing and pressing device and its use method |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102862027B (en) | The electrolysis continuous production technology of special-shaped hollow conductive plate | |
| CN106391741B (en) | A kind of aluminum alloy blade profile and its manufacturing process | |
| CN118681944A (en) | Aluminum profile extrusion die and method | |
| CN110640121A (en) | Grid continuous casting and coating production line | |
| CN107097043A (en) | A kind of manufacture method of 6101 aluminium alloy extrusions | |
| CN102896174B (en) | The electrolysis preparation technology of the hollow conductive plate of continuously extruded abnormal shape | |
| CN116493444A (en) | A 2224 aluminum alloy profile straightening device and a profile processing technology using the straightening device | |
| CN119951900B (en) | An aluminum tube extrusion molding machine | |
| CN113464490A (en) | Mining axial fan wing type blade and machining die thereof | |
| CN119681041A (en) | Aluminum profile processing device and method for high-efficiency extrusion | |
| CN110293143A (en) | A kind of titanium alloy profile hot pull apparatus for shaping and method | |
| CN216911576U (en) | A kind of extrusion machine for aluminum profiles | |
| CN114247753B (en) | Aluminum alloy pipe cold rolling device | |
| CN112247049B (en) | Anti-rotation seat and machining method thereof | |
| CN222001553U (en) | Aluminum alloy profile processing cooling device | |
| CN222241984U (en) | High-strength aluminum alloy girder extrusion die cooling equipment for automobile light weight | |
| CN224208820U (en) | Aluminum profile machining and forming system | |
| CN1966204A (en) | Producing technology for large size copper heterotype plate | |
| CN223368188U (en) | A forming die for producing alloy roller sleeves | |
| CN224170235U (en) | Quick cooling device of elevator handrail area forming die | |
| CN120460520A (en) | Aluminum alloy bar processing device and processing method | |
| CN214056299U (en) | Injection mold frame with good cooling effect | |
| CN222710782U (en) | A production mold for aluminum alloy die castings | |
| CN220804978U (en) | Wire drawing machine for spring production with high heat dissipation | |
| CN223405943U (en) | A uniformly cooled sand casting mold |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination |