CN115635572A - Lamp forming equipment - Google Patents
Lamp forming equipment Download PDFInfo
- Publication number
- CN115635572A CN115635572A CN202011449611.6A CN202011449611A CN115635572A CN 115635572 A CN115635572 A CN 115635572A CN 202011449611 A CN202011449611 A CN 202011449611A CN 115635572 A CN115635572 A CN 115635572A
- Authority
- CN
- China
- Prior art keywords
- wall
- seat
- fixed
- screws
- lamp
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P40/00—Technologies relating to the processing of minerals
- Y02P40/50—Glass production, e.g. reusing waste heat during processing or shaping
- Y02P40/57—Improving the yield, e-g- reduction of reject rates
Landscapes
- Arrangement Of Elements, Cooling, Sealing, Or The Like Of Lighting Devices (AREA)
- Cleaning In General (AREA)
Abstract
Description
技术领域technical field
本发明涉及陶瓷灯加工技术领域,尤其涉及一种灯成型设备。The invention relates to the technical field of ceramic lamp processing, in particular to lamp forming equipment.
背景技术Background technique
在陶瓷灯的加工中,多利用模具将灯坯加工成特定的形状,在脱模时,灯坯表面或多或少的会附着有余料、毛刺等等,为了保障产品的质量,常常对灯坯进行细致性修整,将余料及毛刺切除,而目前用于修整灯坯的设备,虽能够满足一定的使用需求,但是,在切割过程中,易出现偏差,破坏了灯坯的形状,从而带来不同程度的损失。In the processing of ceramic lamps, molds are often used to process lamp blanks into specific shapes. When demoulding, more or less residual materials, burrs, etc. will be attached to the surface of lamp blanks. In order to ensure product quality, lamp blanks are often The blank is carefully trimmed to remove the remaining material and burrs. Although the current equipment for trimming the lamp blank can meet certain usage requirements, it is prone to deviations during the cutting process, which destroys the shape of the lamp blank, thereby causing to varying degrees of loss.
经检索,中国专利申请号为CN201310606286.3的专利,公开了陶瓷坯件的机械切削装置,包括一基座(1),在基座上设置调速电机(2),调速电机(2)上设置陶瓷摆放台(3);设置坯体切削刀具盘(4)、数控控制模块(5),刀具盘(4)上设置不同切削结构的刀具(6),在切削刀具盘(4)边设置监视装置(7),将切割加工的数据输入数控控制模块(5),陶瓷坯体(8)放置在陶瓷摆放台(3),刀具(6)按设定程序对陶瓷坯体进行切削,通过监视装置(7)监控切削进程;在监视装置(7)前设置透明的隔离板(9);设置提示装置(10),对于切削过程中的进展状态进行提示。上述专利中的切削装置存在以下不足:在切割过程中,易出现偏差,破坏了灯坯的形状,从而带来不同程度的损失。After retrieval, the Chinese patent application number is CN201310606286.3, which discloses a mechanical cutting device for ceramic blanks, including a base (1), on which a speed-regulating motor (2) is arranged, and a speed-regulating motor (2) A ceramic placement table (3) is arranged on the top; a green body cutting tool disc (4) and a numerical control module (5) are arranged, and cutters (6) of different cutting structures are arranged on the tool disc (4), and on the cutting tool disc (4) The monitoring device (7) is set up, and the data of cutting processing is input into the numerical control control module (5), and the ceramic body (8) is placed on the ceramic placing table (3), and the cutter (6) performs the process on the ceramic body according to the set program For cutting, monitor the cutting process through the monitoring device (7); set a transparent isolation plate (9) in front of the monitoring device (7); set a prompting device (10) to prompt the progress status during the cutting process. The cutting device in the above-mentioned patent has the following disadvantages: in the cutting process, it is easy to deviate and destroy the shape of the lamp blank, thereby causing losses in different degrees.
发明内容Contents of the invention
本发明的目的是为了解决现有技术中存在的缺点,而提出的一种灯成型设备。The object of the present invention is to propose a lamp shaping device in order to solve the shortcomings in the prior art.
为了实现上述目的,本发明采用了如下技术方案:In order to achieve the above object, the present invention adopts the following technical solutions:
一种灯成型设备,包括基座和用于承托灯坯的转台,所述基座顶部外壁通过螺丝固定有环形滑座,所述转台底部外壁通过螺丝固定有四个以上均匀圆周分布的滑球杆,所述滑球杆底部外壁滑动连接于环形滑座顶部内壁;所述基座顶部外壁通过螺丝固定有安装架,安装架一侧安装有刮刀机构,所述转台上设置有用于给灯坯定位的定位机构,所述定位机构包括中心转杆和四个以上的弧形撑板,所述中心转杆转动连接于转台内壁,且中心转杆与转台的中轴线重合,所述弧形撑板靠近中心转杆一侧内壁与中心转杆圆周外壁之间均焊接有弹力片,转台顶部外壁通过螺丝固定有环形固定座,弹力片贯穿滑动于环形固定座内壁,弹力片构成旋风形结构;所述中心转杆顶端侧壁通过螺丝固定有转柄。A lamp forming device, comprising a base and a turntable for supporting lamp blanks, the top outer wall of the base is fixed with an annular slide seat by screws, and the bottom outer wall of the turntable is fixed with more than four slides evenly distributed around the circumference. The outer wall of the bottom of the sliding club is slidably connected to the inner wall of the top of the ring-shaped sliding seat; the outer wall of the top of the base is fixed with a mounting frame by screws, and a scraper mechanism is installed on one side of the mounting frame. The positioning mechanism for billet positioning, the positioning mechanism includes a central rotating rod and more than four arc-shaped support plates, the central rotating rod is rotatably connected to the inner wall of the turntable, and the central rotating rod coincides with the central axis of the turntable, and the arc-shaped Elastic pieces are welded between the inner wall of the support plate near the central rotating rod and the outer wall of the central rotating rod. The outer wall of the top of the turntable is fixed with a ring-shaped fixing seat by screws. The elastic piece runs through and slides on the inner wall of the ring-shaped fixing seat. ; The top side wall of the central rotating rod is fixed with a rotating handle by screws.
优选的:所述中心转杆圆周外壁通过螺丝固定有环形齿座,转台底部外壁通过螺丝固定有四个以上的滑筒,滑筒内壁均滑动连接有滑杆,滑杆顶部外壁与滑筒顶部内壁之间焊接有同一个滑杆弹簧;滑杆底端通过螺丝固定有同一个连接环,连接环靠近中心转杆的圆周内壁上通过螺丝固定有两个以上等距分布的单向挡柱,所述单向挡柱与环形齿座适配,所述单向挡柱靠近环形齿座的一端外壁转动安装有空心滚柱;连接环一侧外壁通过螺丝固定有踏杆,踏杆一端一体式设置有踏板。Preferably: the peripheral outer wall of the central rotating rod is fixed with an annular gear seat, the outer wall of the bottom of the turntable is fixed with more than four sliding cylinders through screws, the inner walls of the sliding cylinders are all slidably connected with sliding rods, and the outer wall of the top of the sliding rod is connected to the top of the sliding cylinder. The same slide bar spring is welded between the inner walls; the bottom end of the slide bar is fixed with the same connecting ring by screws, and two or more equidistant one-way retaining columns are fixed by screws on the inner wall of the circumference of the connecting ring close to the center rotating rod. The one-way retaining column is adapted to the annular tooth seat, and the outer wall of one end of the one-way retaining column close to the annular tooth seat is rotatably installed with a hollow roller; the outer wall on one side of the connecting ring is fixed with a pedal rod, and one end of the pedal rod is integrated Set with pedals.
进一步的:所述滑球杆靠近中心转杆的一侧外壁通过螺丝固定有同一个连接架,连接架顶部外壁一体式设置有凸环,凸环位于中心转杆底端外侧且与中心转杆同心,中心转杆底端侧壁与连接架的凸环内壁焊接有同一个涡卷弹簧。Further: the outer wall of the side of the sliding club close to the central rotating rod is fixed with the same connecting frame by screws, and the outer wall on the top of the connecting frame is integrally provided with a convex ring, which is located outside the bottom end of the central rotating rod and connected to the central rotating rod. Concentric, the side wall at the bottom end of the central rotating rod and the inner wall of the convex ring of the connecting frame are welded with the same scroll spring.
进一步优选的:所述弧形撑板一侧外壁嵌入式安装有两个以上的空心胶条。Further preferably: two or more hollow rubber strips are embedded in one side of the outer wall of the arc-shaped support plate.
作为本发明一种优选的:所述刮刀机构包括刮刀和刮刀座,所述安装架两侧内壁转动安装有同一个升降螺杆,升降螺杆顶端贯穿安装架后通过螺丝固定有升降旋钮,所述升降螺杆通过螺纹连接有升降块,升降块一侧外壁通过压力调节机构安装有调节座,所述调节座一端内壁滑动连接有调节杆,且调节座顶部内壁通过螺纹连接有用于固定调节杆的水平调节旋钮,所述调节杆一端内壁转动连接有转杆,调节杆一端顶部内壁通过螺纹连接有用于固定转杆的角度调节旋钮,所述刮刀通过螺丝固定于刮刀座一侧外壁,转杆一端外壁通过螺丝固定于刮刀座的另一侧外壁。As a preferred aspect of the present invention: the scraper mechanism includes a scraper and a scraper seat, the inner walls on both sides of the mounting frame are rotatably mounted with the same lifting screw, and the top of the lifting screw penetrates the mounting frame and is fixed with a lifting knob by a screw. The screw rod is connected with a lifting block through a thread, and the outer wall of one side of the lifting block is installed with an adjustment seat through a pressure adjustment mechanism. The inner wall of one end of the adjustment seat is slidingly connected with an adjustment rod, and the inner wall of the top of the adjustment seat is connected with a horizontal adjustment for fixing the adjustment rod through a thread. Knob, the inner wall at one end of the adjusting rod is rotatably connected with a rotating rod, the inner wall at the top of one end of the adjusting rod is threadedly connected with an angle adjustment knob for fixing the rotating rod, the scraper is fixed on the outer wall on one side of the scraper seat by screws, and the outer wall at one end of the rotating rod is passed through The screw is fixed on the other side outer wall of the scraper seat.
作为本发明进一步优选的:所述压力调节机构包括弹性胶套和限位气囊,所述调节座一侧设置有导向柱,导向柱一端通过螺丝固定有胶套安装板,所述导向柱外壁滑动连接有导向座,导向座外壁滑动连接有滑动板,弹性胶套两端外壁分别粘接于滑动板一侧外壁和胶套安装板的一侧外壁,所述限位气囊套于导向座外部,且导向座位于升降块和滑动板之间;所述限位气囊顶部外壁通过气管接有带气阀的调节气囊,所述调节气囊通过卡扣固定于安装架一侧外壁。As a further preferred aspect of the present invention: the pressure regulating mechanism includes an elastic rubber sleeve and a limit air bag, a guide column is arranged on one side of the adjustment seat, and a rubber sleeve mounting plate is fixed at one end of the guide column by screws, and the outer wall of the guide column slides A guide seat is connected, the outer wall of the guide seat is slidably connected with a sliding plate, and the outer walls at both ends of the elastic rubber sleeve are respectively bonded to one side of the outer wall of the sliding plate and one side of the rubber sleeve installation plate, and the limit airbag is set outside the guide seat. And the guide seat is located between the lifting block and the sliding plate; the top outer wall of the spacer air bag is connected with an air valve regulating air bag through a trachea, and the regulating air bag is fixed on the outer wall of one side of the mounting bracket through a buckle.
作为本发明再进一步的方案:所述调节座一端外壁与胶套安装板一侧外壁之间安装有同一个压力传感组件,所述调节座一侧外壁通过螺丝固定有压力表,压力表与压力传感组件电性连接。As a further solution of the present invention: the same pressure sensing component is installed between the outer wall at one end of the adjustment seat and the outer wall at one side of the rubber sleeve mounting plate, and a pressure gauge is fixed on the outer wall at one side of the adjustment seat through screws, and the pressure gauge and The pressure sensing component is electrically connected.
在前述方案的基础上:所述刮刀座为罩型结构,且刮刀座一侧内壁与刮刀一侧外壁相切,基座顶部外壁设置有吸尘装置,刮刀座底部外壁通,负压管接于吸尘装置的输入端。On the basis of the aforementioned scheme: the scraper seat is a cover-shaped structure, and the inner wall on one side of the scraper seat is tangent to the outer wall on one side of the scraper, the outer wall on the top of the base is provided with a dust suction device, the outer wall of the bottom of the scraper seat is connected, and the negative pressure pipe is connected. At the input end of the dust collection device.
在前述方案的基础上优选的:所述基座顶部外壁通过螺丝固定有清洁架,所述清洁架一侧内壁滑动连接有均匀分布的清洁杆,所述清洁杆靠近灯坯的一端外壁均设置有刷头。On the basis of the foregoing solution, preferably: the outer wall of the top of the base is fixed with a cleaning frame by screws, and the inner wall on one side of the cleaning frame is slidably connected with evenly distributed cleaning rods, and the outer wall of one end of the cleaning rods close to the lamp blank is provided. With brush head.
在前述方案的基础上进一步优选的:所述清洁杆外壁均通过螺丝固定有环形板,环形板一侧外壁与清洁架一侧外壁之间均焊接有清洁弹簧。On the basis of the foregoing solution, it is further preferred that the outer walls of the cleaning rods are all fixed with ring plates by screws, and cleaning springs are welded between the outer walls of one side of the ring plate and the outer wall of one side of the cleaning frame.
一种灯成型工艺,包括如下步骤:A lamp forming process, comprising the steps of:
S1:按重量分取坯体原料,化浆后制备成泥条;S1: Divide green body raw materials according to weight, and make mud sticks after pulping;
S2:将制备的进行真空粗炼;S2: Vacuum roughing the prepared one;
S3:将真空粗炼后的泥条利用真空练泥机二次挤压练泥;S3: Squeeze and refine the mud strips after vacuum roughing by using a vacuum mud refining machine for the second time;
S4:将得到的泥料按需切入不锈钢模中;S4: cutting the obtained mud into stainless steel molds as required;
S5:将含有泥料的钢模输送到对辊压制设备进行压制;S5: Transport the steel mold containing mud to the roller pressing equipment for pressing;
S6:压制后的钢模置于烤房中烤坯后脱模,得到灯坯;S6: the pressed steel mold is placed in a baking room to bake the billet, and then demolded to obtain a lamp billet;
S7:将灯坯通过上述消防疏散陶瓷灯成型设备进行处理;S7: Processing the lamp blank through the above-mentioned fire evacuation ceramic lamp forming equipment;
S8:将处理后的灯坯依次进行淋釉、印花、釉烧处理,得到陶瓷灯产品;S8: The processed lamp blanks are sequentially subjected to glazing, printing, and glaze firing treatments to obtain ceramic lamp products;
S9:将陶瓷灯产品分级包装。S9: Packing the ceramic lamp products in grades.
优选的:所述S1步骤中,坯体原料按重量份计,包括特级高岭土30~35份、钾长石50~55份、超细石英10~15份、氧化铝粉体5~7.5份、増白剂2~3份、増塑剂3~5份。Preferably: in the step S1, the green body raw materials include 30-35 parts by weight of super-grade kaolin, 50-55 parts of potassium feldspar, 10-15 parts of ultrafine quartz, 5-7.5 parts of alumina powder, 2-3 parts of whitening agent, 3-5 parts of plasticizer.
进一步的:所述S1步骤中,将坯体原料的成分控制为:SiO2 64.30%,Al2O3 17~20%、Fe2O3<0.1%、CaO 0.45~0.75%、MgO 0.25~0.4%、TiO2<0.05%、K2O 6~7%、Na2O1~1.5%、其他2~3%,烧失量控制在5~6%。Further: in the S1 step, the components of the green body raw materials are controlled as: SiO 2 64.30%, Al 2 O 3 17-20%, Fe 2 O 3 <0.1%, CaO 0.45-0.75%, MgO 0.25-0.4 %, TiO 2 <0.05%, K 2 O 6-7%, Na 2 O 1-1.5%, other 2-3%, and the loss on ignition is controlled at 5-6%.
进一步优选的:所述氧化铝粉体添加量占坯体原料总质量的4.5~7%。Further preferably: the added amount of the alumina powder accounts for 4.5-7% of the total mass of the green body raw materials.
作为本发明一种优选的:所述S3步骤中,真空练泥机的挤出旋转轴的转速控制在20~25r/min,真空度控制在98%以上。As a preferred embodiment of the present invention: in the step S3, the rotation speed of the extrusion rotating shaft of the vacuum mud mill is controlled at 20-25 r/min, and the vacuum degree is controlled at above 98%.
作为本发明进一步优选的:所述S6步骤中,在烤房中进行烤坯时,将坯体用耐火纸包裹后进行烤坯,烤坯的温度控制在1050~1125℃,烤坯后保温2~3h。As a further preferred aspect of the present invention: in the step S6, when the green body is baked in the baking room, the green body is wrapped with fireproof paper and then baked. ~3h.
作为本发明再进一步的方案:所述S8步骤中,在进行淋釉之前还需将处理后的灯坯通过制动洗水机洗水,并将洗水后的灯坯送入烤房进行二次烤坯,经二次烤坯后再进行淋釉操作。As a further solution of the present invention: in the step S8, the treated lamp blanks need to be washed by a braking water washing machine before being glazed, and the washed lamp blanks are sent to the baking room for two After the second baking, the glaze is poured after the second baking.
在前述方案的基础上:所述S8步骤中,二次烤坯的温度控制在1075~1100℃。On the basis of the aforementioned solution: in the step S8, the temperature of the secondary baking body is controlled at 1075-1100°C.
在前述方案的基础上优选的:将所述S1步骤中,的坯体原料进一步限定为:特级高岭土32~33份、钾长石52~54份、超细石英11~13份、氧化铝粉体6~7份、増白剂3份、増塑剂4份。On the basis of the aforementioned scheme, preferably: in the step S1, the green body raw materials are further limited to: 32-33 parts of super-grade kaolin, 52-54 parts of potassium feldspar, 11-13 parts of ultrafine quartz, alumina powder 6-7 parts of body, 3 parts of whitening agent, 4 parts of plasticizer.
在前述方案的基础上进一步优选的:所述氧化铝粉体添加量进一步限定为占坯体原料总质量的6%。On the basis of the foregoing solution, it is further preferred that the addition amount of the alumina powder is further limited to 6% of the total mass of the green body raw materials.
本发明的有益效果为:The beneficial effects of the present invention are:
1.本发明通过设置转台、滑球杆等结构,能够便于将灯坯置于转台上,以转动转台的方式使灯坯的圆周侧壁与刮刀机构接触,从而避免了切割不均匀的现象,提升了切割效果,此外,由于采用旋风形结构的弹力片,通过旋转中心转杆,在环形固定座的限位下,使得弹力片一端远离中心转杆,从而使弧形撑板向外扩张,中心转杆转动到一定程度后,弧形撑板接触并顶撑于灯坯的内壁,以达到固定的效果,该设计能够适应于不同尺寸的灯坯,保障了设备的泛用性。1. The present invention can easily place the lamp blank on the turntable by setting a turntable, a sliding club, etc., and make the circumferential side wall of the lamp blank contact with the scraper mechanism by rotating the turntable, thereby avoiding the phenomenon of uneven cutting. The cutting effect is improved. In addition, due to the use of the elastic sheet with a whirlwind structure, by rotating the central rotating rod, under the limit of the annular fixed seat, one end of the elastic sheet is away from the central rotating rod, so that the arc-shaped support plate expands outward. After the central rotating rod rotates to a certain extent, the arc-shaped support plate contacts and supports the inner wall of the lamp blank to achieve a fixed effect. This design can be adapted to different sizes of lamp blanks, ensuring the versatility of the equipment.
2.通过设置单向挡柱、滑筒和滑杆等结构,能够利用单向挡柱一端伸入环形齿座内,当中心转杆转动时,空心滚柱在环形齿座的导向下滑动于环形齿座齿面上,滑杆在滑杆弹簧形变下滑动于滑筒内,进而连接环得以起伏升降,以配合空心滚柱的滑动,当中心转杆向被限制的方向转动时,空心滚柱阻挡于环形齿座齿面一侧,从而与环形齿座配合构成单向限制中心转杆转动方向的效果,有效避免了弹力片回弹,通过设置空心滚柱,保障了限制效果的同时,提升了中心转杆转动的流畅度。2. By setting up one-way blocking column, sliding cylinder and sliding rod and other structures, one end of the one-way blocking column can be used to extend into the ring tooth seat. When the central rotating rod rotates, the hollow roller slides on the ring under the guidance of the ring tooth seat. On the tooth surface of the ring tooth seat, the slide bar slides in the slide tube under the deformation of the slide bar spring, and then the connecting ring can rise and fall to match the sliding of the hollow roller. The column is blocked on one side of the tooth surface of the ring tooth seat, so that it cooperates with the ring tooth seat to form a one-way effect of restricting the rotation direction of the central rotating rod, effectively avoiding the rebound of the elastic sheet. By setting the hollow roller, the restriction effect is guaranteed. The smoothness of the rotation of the center rotating rod has been improved.
3.通过设置涡卷弹簧,能够利用下压踏板使得单向挡柱脱离环形齿座,进而在涡卷弹簧的作用下使得中心转杆和转柄得以复位,操作简单可靠,提升了实用性;通过设置空心胶条,能够在弧形撑板接触灯坯内壁时,利用空心胶条的形变增大与灯坯之间的摩擦力,进而提升固定效果,保障了可靠性。3. By setting the scroll spring, the one-way retaining column can be separated from the ring tooth seat by pressing down the pedal, and then the center rotating rod and the rotating handle can be reset under the action of the scroll spring. The operation is simple and reliable, and the practicability is improved; By arranging the hollow rubber strip, when the arc-shaped support plate contacts the inner wall of the lamp blank, the deformation of the hollow rubber strip can be used to increase the friction between the lamp blank and the lamp blank, thereby improving the fixing effect and ensuring the reliability.
4.通过设置升降旋钮、水平调节旋钮、角度调节旋钮等结构,能够便于对刮刀进行多方位调节,从而使得其能够适应不同形状尺寸的灯坯,提升了灵活性和泛用性。4. By setting up and down knobs, horizontal adjustment knobs, angle adjustment knobs and other structures, the scraper can be adjusted in multiple directions, so that it can adapt to lamp blanks of different shapes and sizes, improving flexibility and versatility.
5.通过设置限位气囊、弹性胶套等结构,能够利用调节气囊调节限位气囊的体积,进而改变升降块与滑动板的间距,并在弹性胶套形变缓冲的配合下,使得刮刀能够充分与灯坯外壁接触,从而提升了切削的可靠性,由于限位气囊可调,因此能够更好的满足使用者的使用需求。5. By setting the limit air bag, elastic rubber sleeve and other structures, the volume of the limit air bag can be adjusted by adjusting the air bag, and then the distance between the lifting block and the sliding plate can be changed, and with the cooperation of the deformation buffer of the elastic rubber sleeve, the scraper can fully It is in contact with the outer wall of the lamp blank, thereby improving the reliability of cutting. Since the limit airbag is adjustable, it can better meet the needs of users.
6.通过设置压力传感组件和压力表,能够直观的了解刮刀与灯坯外壁之间的作用力,从而利于通过调节气囊更好的进行调节,提升了实用性;通过设置刮刀座、吸尘装置等结构,能够对刮刀刮下的废料进行实时收集处理,提升了环保性和实用性。6. By setting the pressure sensing component and the pressure gauge, it is possible to intuitively understand the force between the scraper and the outer wall of the lamp blank, which is conducive to better adjustment by adjusting the air bag and improving the practicability; by setting the scraper seat, dust suction The device and other structures can collect and process the waste scraped by the scraper in real time, which improves environmental protection and practicability.
7.通过设置刷头,能够基于转台带动灯坯转动,同步对灯坯表面进行擦拭,提升灯坯的洁净度,利于进一步的加工;通过设置清洁弹簧和环形板,能够增强刷头的清洁力度,从而提升清洁效果。7. By setting the brush head, the lamp blank can be driven to rotate based on the turntable, and the surface of the lamp blank can be wiped synchronously to improve the cleanliness of the lamp blank, which is beneficial to further processing; by setting the cleaning spring and the ring plate, the cleaning power of the brush head can be enhanced , thereby improving the cleaning effect.
附图说明Description of drawings
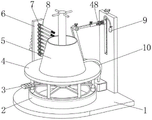
图1为本发明提出的一种灯成型设备整体的结构示意图;Fig. 1 is a schematic diagram of the overall structure of a lamp forming device proposed by the present invention;
图2为本发明提出的一种灯成型设备另一侧的结构示意图;Fig. 2 is a structural schematic diagram of the other side of a lamp forming device proposed by the present invention;
图3为本发明提出的一种灯成型设备转台的结构示意图;Fig. 3 is a structural schematic diagram of a lamp forming equipment turntable proposed by the present invention;
图4为本发明提出的一种灯成型设备转台剖视的结构示意图;Fig. 4 is a structural schematic diagram of a sectional view of a turntable of a lamp forming equipment proposed by the present invention;
图5为本发明提出的一种灯成型设备环形齿座的结构示意图;Fig. 5 is a structural schematic diagram of an annular tooth seat of a lamp forming equipment proposed by the present invention;
图6为本发明提出的一种灯成型设备刮刀座的结构示意图;Fig. 6 is a schematic structural view of a lamp forming equipment scraper seat proposed by the present invention;
图7为本发明提出的一种灯成型设备调节座剖视的结构示意图;Fig. 7 is a structural schematic diagram of a cross-sectional view of an adjusting seat of a lamp forming equipment proposed by the present invention;
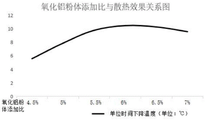
图8为本发明提出的一种灯成型工艺中的氧化铝粉体添加比与散热效果关系图。Fig. 8 is a graph showing the relationship between the addition ratio of alumina powder and the heat dissipation effect in a lamp forming process proposed by the present invention.
图中:1基座、2环形滑座、3踏板、4转台、5灯坯、6清洁架、7清洁弹簧、8环形板、9调节气囊、10负压管、11安装架、12升降螺杆、13刮刀座、14升降块、15升降旋钮、16刷头、17清洁杆、18吸尘装置、19环形固定座、20弹力片、21中心转杆、22转柄、23弧形撑板、24滑球杆、25空心胶条、26连接环、27滑杆弹簧、28单向挡柱、29涡卷弹簧、30滑杆、31连接架、32踏杆、33滑筒、34空心滚柱、35环形齿座、36调节座、37弹性胶套、38限位气囊、39气管、40水平调节旋钮、41调节杆、42角度调节旋钮、43转杆、44刮刀、45导向柱、46导向座、47滑动板、48压力表、49压力传感组件。In the figure: 1 base, 2 annular sliding seat, 3 pedal, 4 turntable, 5 lamp blank, 6 cleaning frame, 7 cleaning spring, 8 annular plate, 9 adjusting air bag, 10 negative pressure tube, 11 mounting frame, 12 lifting screw , 13 scraper seat, 14 lifting block, 15 lifting knob, 16 brush head, 17 cleaning rod, 18 vacuum device, 19 ring fixing seat, 20 elastic piece, 21 center rotating rod, 22 rotating handle, 23 arc support plate, 24 sliding club, 25 hollow rubber strip, 26 connecting ring, 27 sliding rod spring, 28 one-way retaining column, 29 scroll spring, 30 sliding rod, 31 connecting frame, 32 pedal rod, 33 sliding cylinder, 34 hollow roller , 35 ring gear seat, 36 adjustment seat, 37 elastic rubber sleeve, 38 limit air bag, 39 air pipe, 40 level adjustment knob, 41 adjustment rod, 42 angle adjustment knob, 43 rotating rod, 44 scraper, 45 guide column, 46 guide Seat, 47 sliding plates, 48 pressure gauges, 49 pressure sensing components.
具体实施方式Detailed ways
下面结合具体实施方式对本专利的技术方案作进一步详细地说明。The technical solution of this patent will be further described in detail below in conjunction with specific embodiments.
下面详细描述本专利的实施例,所述实施例的示例在附图中示出,其中自始至终相同或类似的标号表示相同或类似的元件或具有相同或类似功能的元件。下面通过参考附图描述的实施例是示例性的,仅用于解释本专利,而不能理解为对本专利的限制。Embodiments of the present patent are described in detail below, examples of which are shown in the drawings, wherein the same or similar reference numerals designate the same or similar elements or elements having the same or similar functions throughout. The embodiments described below by referring to the figures are exemplary and are only used for explaining the patent, and should not be construed as limiting the patent.
在本专利的描述中,需要理解的是,术语“中心”、“上”、“下”、“前”、“后”、“左”、“右”、“竖直”、“水平”、“顶”、“底”、“内”、“外”等指示的方位或位置关系为基于附图所示的方位或位置关系,仅是为了便于描述本专利和简化描述,而不是指示或暗示所指的装置或元件必须具有特定的方位、以特定的方位构造和操作,因此不能理解为对本专利的限制。In the description of this patent, it is to be understood that the terms "center", "upper", "lower", "front", "rear", "left", "right", "vertical", "horizontal", The orientation or positional relationship indicated by "top", "bottom", "inner", "outer", etc. is based on the orientation or positional relationship shown in the drawings, and is only for the convenience of describing this patent and simplifying the description, rather than indicating or implying References to devices or elements must have a particular orientation, be constructed, and operate in a particular orientation and therefore should not be construed as limiting on the patent.
在本专利的描述中,需要说明的是,除非另有明确的规定和限定,术语“安装”、“相连”、“连接”、“设置”应做广义理解,例如,可以是固定相连、设置,也可以是可拆卸连接、设置,或一体地连接、设置。对于本领域的普通技术人员而言,可以根据具体情况理解上述术语在本专利中的具体含义。In the description of this patent, it should be noted that, unless otherwise clearly specified and limited, the terms "installation", "connection", "connection", and "setting" should be understood in a broad sense, for example, it can be fixed connection, setting , can also be detachably connected and set, or integrally connected and set. Those of ordinary skill in the art can understand the specific meanings of the above terms in this patent according to specific situations.
实施例1:Example 1:
一种灯成型设备,如图1-7所示,包括基座1和用于承托灯坯5的转台4,所述基座1顶部外壁通过螺丝固定有环形滑座2,所述转台4底部外壁通过螺丝固定有四个以上均匀圆周分布的滑球杆24,所述滑球杆24底部外壁滑动连接于环形滑座2顶部内壁;所述基座1顶部外壁通过螺丝固定有安装架11,安装架11一侧安装有刮刀机构,所述转台4上设置有用于给灯坯5定位的定位机构,所述定位机构包括中心转杆21和四个以上的弧形撑板23,所述中心转杆21转动连接于转台4内壁,且中心转杆21与转台4的中轴线重合,所述弧形撑板23靠近中心转杆21一侧内壁与中心转杆21圆周外壁之间均焊接有弹力片20,转台4顶部外壁通过螺丝固定有环形固定座19,弹力片20贯穿滑动于环形固定座19内壁,弹力片20构成旋风形结构;所述中心转杆21顶端侧壁通过螺丝固定有转柄22;通过设置转台4、滑球杆24等结构,能够便于将灯坯5置于转台4上,以转动转台4的方式使灯坯5的圆周侧壁与刮刀机构接触,从而避免了切割不均匀的现象,提升了切割效果,此外,由于采用旋风形结构的弹力片20,通过旋转中心转杆21,在环形固定座19的限位下,使得弹力片20一端远离中心转杆21,从而使弧形撑板23向外扩张,中心转杆21转动到一定程度后,弧形撑板23接触并顶撑于灯坯5的内壁,以达到固定的效果,该设计能够适应于不同尺寸的灯坯5,保障了设备的泛用性。A lamp forming equipment, as shown in Figure 1-7, includes a
为了避免弹力片20回弹;如图3-5所示,所述中心转杆21圆周外壁通过螺丝固定有环形齿座35,转台4底部外壁通过螺丝固定有四个以上的滑筒33,滑筒33内壁均滑动连接有滑杆30,滑杆30顶部外壁与滑筒33顶部内壁之间焊接有同一个滑杆弹簧27;滑杆30底端通过螺丝固定有同一个连接环26,连接环26靠近中心转杆21的圆周内壁上通过螺丝固定有两个以上等距分布的单向挡柱28,所述单向挡柱28与环形齿座35适配,所述单向挡柱28靠近环形齿座35的一端外壁转动安装有空心滚柱34;连接环26一侧外壁通过螺丝固定有踏杆32,踏杆32一端一体式设置有踏板3;通过设置单向挡柱28、滑筒33和滑杆30等结构,能够利用单向挡柱28一端伸入环形齿座35内,当中心转杆21转动时,空心滚柱34在环形齿座35的导向下滑动于环形齿座35齿面上,滑杆30在滑杆弹簧27形变下滑动于滑筒33内,进而连接环26得以起伏升降,以配合空心滚柱34的滑动,当中心转杆21向被限制的方向转动时,空心滚柱34阻挡于环形齿座35齿面一侧,从而与环形齿座35配合构成单向限制中心转杆21转动方向的效果,有效避免了弹力片20回弹,通过设置空心滚柱34,保障了限制效果的同时,提升了中心转杆21转动的流畅度。In order to avoid
为了便于中心转杆21的复位;如图4、图5所示,所述滑球杆24靠近中心转杆21的一侧外壁通过螺丝固定有同一个连接架31,连接架31顶部外壁一体式设置有凸环,凸环位于中心转杆21底端外侧且与中心转杆21同心,中心转杆21底端侧壁与连接架31的凸环内壁焊接有同一个涡卷弹簧29;通过设置涡卷弹簧29,能够利用下压踏板3使得单向挡柱28脱离环形齿座35,进而在涡卷弹簧29的作用下使得中心转杆21和转柄22得以复位,操作简单可靠,提升了实用性。In order to facilitate the reset of the central
为了提升固定效果;如图4所示,所述弧形撑板23一侧外壁嵌入式安装有两个以上的空心胶条25;通过设置空心胶条25,能够在弧形撑板23接触灯坯5内壁时,利用空心胶条25的形变增大与灯坯5之间的摩擦力,进而提升固定效果,保障了可靠性。In order to improve the fixing effect; as shown in Figure 4, more than two hollow rubber strips 25 are embedded in the outer wall of one side of the
为了便于切割余料及毛边;如图2、图6、图7所示,所述刮刀机构包括刮刀44和刮刀座13,所述安装架11两侧内壁转动安装有同一个升降螺杆12,升降螺杆12顶端贯穿安装架11后通过螺丝固定有升降旋钮15,所述升降螺杆12通过螺纹连接有升降块14,升降块14一侧外壁通过压力调节机构安装有调节座36,所述调节座36一端内壁滑动连接有调节杆41,且调节座36顶部内壁通过螺纹连接有用于固定调节杆41的水平调节旋钮40,所述调节杆41一端内壁转动连接有转杆43,调节杆41一端顶部内壁通过螺纹连接有用于固定转杆43的角度调节旋钮42,所述刮刀44通过螺丝固定于刮刀座13一侧外壁,转杆43一端外壁通过螺丝固定于刮刀座13的另一侧外壁;通过设置升降旋钮15、水平调节旋钮40、角度调节旋钮42等结构,能够便于对刮刀44进行多方位调节,从而使得其能够适应不同形状尺寸的灯坯5,提升了灵活性和泛用性。In order to facilitate the cutting of surplus materials and burrs; as shown in Figure 2, Figure 6, and Figure 7, the scraper mechanism includes a
为了便于调节;如图6、图7所示,所述压力调节机构包括弹性胶套37和限位气囊38,所述调节座36一侧设置有导向柱45,导向柱45一端通过螺丝固定有胶套安装板,所述导向柱45外壁滑动连接有导向座46,导向座46外壁滑动连接有滑动板47,弹性胶套37两端外壁分别粘接于滑动板47一侧外壁和胶套安装板的一侧外壁,所述限位气囊38套于导向座46外部,且导向座46位于升降块14和滑动板47之间;所述限位气囊38顶部外壁通过气管39接有带气阀的调节气囊9,所述调节气囊9通过卡扣固定于安装架11一侧外壁;通过设置限位气囊38、弹性胶套37等结构,能够利用调节气囊9调节限位气囊38的体积,进而改变升降块14与滑动板47的间距,并在弹性胶套37形变缓冲的配合下,使得刮刀44能够充分与灯坯5外壁接触,从而提升了切削的可靠性,由于限位气囊38可调,因此能够更好的满足使用者的使用需求。In order to facilitate adjustment; as shown in Fig. 6 and Fig. 7, the pressure regulating mechanism includes an
为了提升实用性;如图1、图7所示,所述调节座36一端外壁与胶套安装板一侧外壁之间安装有同一个压力传感组件49,所述压力传感组件49中压力传感器的型号可采用PT124G-111;所述调节座36一侧外壁通过螺丝固定有压力表48,压力表48与压力传感组件49电性连接;通过设置压力传感组件49和压力表48,能够直观的了解刮刀44与灯坯5外壁之间的作用力,从而利于通过调节气囊9更好的进行调节,提升了实用性。In order to improve practicality; as shown in Figure 1 and Figure 7, the same
为了便于收集废料;如图2、图6所示,所述刮刀座13为罩型结构,且刮刀座13一侧内壁与刮刀44一侧外壁相切,基座1顶部外壁设置有吸尘装置18,刮刀座13底部外壁通,负压管10接于吸尘装置18的输入端;通过设置刮刀座13、吸尘装置18等结构,能够对刮刀44刮下的废料进行实时收集处理,提升了环保性和实用性。In order to facilitate the collection of waste; as shown in Figure 2 and Figure 6, the
为了便于清洁灯坯5表面;如图1、图2所示,所述基座1顶部外壁通过螺丝固定有清洁架6,所述清洁架6一侧内壁滑动连接有均匀分布的清洁杆17,所述清洁杆17靠近灯坯5的一端外壁均设置有刷头16;通过设置刷头16,能够基于转台4带动灯坯5转动,同步对灯坯5表面进行擦拭,提升灯坯5的洁净度,利于进一步的加工。In order to facilitate the cleaning of the surface of the
为了提升清洁效果;如图1所示,所述清洁杆17外壁均通过螺丝固定有环形板8,环形板8一侧外壁与清洁架6一侧外壁之间均焊接有清洁弹簧7;通过设置清洁弹簧7和环形板8,能够增强刷头16的清洁力度,从而提升清洁效果。In order to improve the cleaning effect; as shown in Figure 1, the outer wall of the cleaning
本实施例在使用时,使用者将待处理的灯坯5置于转台4上,并通过转柄22旋转中心转杆21,在环形固定座19的限位下,使得弹力片20一端远离中心转杆21,从而使弧形撑板23向外扩张,中心转杆21转动到一定程度后,弧形撑板23接触并顶撑于灯坯5的内壁,以达到固定灯坯5的效果,使用者以转动转台4的方式使灯坯5的圆周侧壁与刮刀机构接触,从而避免了切割不均匀的现象,提升了切割效果;在转动中心转杆21过程中,空心滚柱34在环形齿座35的导向下滑动于环形齿座35齿面上,滑杆30在滑杆弹簧27形变下滑动于滑筒33内,进而连接环26得以起伏升降,以配合空心滚柱34的滑动,当中心转杆21向被限制的方向转动时,空心滚柱34阻挡于环形齿座35齿面一侧,从而与环形齿座35配合构成单向限制中心转杆21转动方向的效果,以避免弹力片20回弹;带需要取下灯坯5时,能够利用下压踏板3使得单向挡柱28脱离环形齿座35,进而在涡卷弹簧29的作用下使得中心转杆21和转柄22得以复位,此外,通过设置升降旋钮15、水平调节旋钮40、角度调节旋钮42等结构,能够便于对刮刀44进行多方位调节,从而使得其能够适应不同形状尺寸的灯坯5,通过设置限位气囊38、弹性胶套37等结构,能够利用调节气囊9调节限位气囊38的体积,进而改变升降块14与滑动板47的间距,并在弹性胶套37形变缓冲的配合下,使得刮刀44能够充分与灯坯5外壁接触,从而提升了切削的可靠性,由于限位气囊38可调,因此能够更好的满足使用者的使用需求;通过设置刷头16,能够基于转台4带动灯坯5转动,同步对灯坯5表面进行擦拭,提升灯坯5的洁净度,利于进一步的加工。When using this embodiment, the user puts the lamp blank 5 to be processed on the
实施例2:Example 2:
一种灯成型工艺,如图1-8所示,包括如下步骤:A lamp forming process, as shown in Figure 1-8, includes the following steps:
S1:按重量分取坯体原料,化浆后制备成泥条;S1: Divide green body raw materials according to weight, and make mud sticks after pulping;
S2:将制备的进行真空粗炼;S2: Vacuum roughing the prepared one;
S3:将真空粗炼后的泥条利用真空练泥机二次挤压练泥;S3: Squeeze and refine the mud strips after vacuum roughing by using a vacuum mud refining machine for the second time;
S4:将得到的泥料按需切入不锈钢模中;S4: cutting the obtained mud into stainless steel molds as required;
S5:将含有泥料的钢模输送到对辊压制设备进行压制;S5: Transport the steel mold containing mud to the roller pressing equipment for pressing;
S6:压制后的钢模置于烤房中烤坯后脱模,得到灯坯5;S6: the pressed steel mold is placed in a baking room to bake the billet and then demolded to obtain the
S7:将灯坯5通过实施例1所述的消防疏散陶瓷灯成型设备进行处理;S7: Process the lamp blank 5 through the fire evacuation ceramic lamp molding equipment described in
S8:将处理后的灯坯5依次进行淋釉、印花、釉烧处理,得到陶瓷灯产品;S8: Carrying out glazing, printing, and glazing treatment on the treated lamp blank 5 in sequence to obtain a ceramic lamp product;
S9:将陶瓷灯产品分级包装。S9: Packing the ceramic lamp products in grades.
其中,所述S1步骤中,坯体原料按重量份计,包括特级高岭土30~35份、钾长石50~55份、超细石英10~15份、氧化铝粉体5~7.5份、増白剂2~3份、増塑剂3~5份。Wherein, in the S1 step, the green body raw materials include 30-35 parts by weight of super-grade kaolin, 50-55 parts of potassium feldspar, 10-15 parts of ultrafine quartz, 5-7.5 parts of alumina powder, 2-3 parts of whitening agent, 3-5 parts of plasticizer.
其中,所述S1步骤中,将坯体原料的成分控制为:SiO2 64.30%,Al2O3 17~20%、Fe2O3<0.1%、CaO 0.45~0.75%、MgO 0.25~0.4%、TiO2<0.05%、K2O 6~7%、Na2O 1~1.5%、其他2~3%,烧失量控制在5~6%。Wherein, in the S1 step, the components of the green body raw materials are controlled as: SiO 2 64.30%, Al 2 O 3 17-20%, Fe 2 O 3 <0.1%, CaO 0.45-0.75%, MgO 0.25-0.4% , TiO 2 <0.05%, K 2 O 6-7%, Na 2 O 1-1.5%, others 2-3%, and the loss on ignition is controlled at 5-6%.
其中,所述氧化铝粉体添加量占坯体原料总质量的4.5~7%。Wherein, the amount of the alumina powder added accounts for 4.5-7% of the total mass of the green body raw materials.
其中,所述S3步骤中,真空练泥机的挤出旋转轴的转速控制在20~25r/min,真空度控制在98%以上。Wherein, in the step S3, the rotational speed of the extrusion rotary shaft of the vacuum mud mill is controlled at 20-25 r/min, and the vacuum degree is controlled at above 98%.
其中,所述S6步骤中,在烤房中进行烤坯时,将坯体用耐火纸包裹后进行烤坯,烤坯的温度控制在1050~1125℃,烤坯后保温2~3h。Wherein, in the step S6, when the green body is baked in the baking room, the green body is wrapped with fireproof paper and then baked. The temperature of the baked green body is controlled at 1050-1125°C, and the green body is kept for 2-3 hours after baking.
其中,所述S8步骤中,在进行淋釉之前还需将处理后的灯坯5通过制动洗水机洗水,并将洗水后的灯坯5送入烤房进行二次烤坯,经二次烤坯后再进行淋釉操作。Wherein, in the step S8, the treated lamp blank 5 needs to be washed by a brake washing machine before the glaze is applied, and the washed
其中,所述S8步骤中,二次烤坯的温度控制在1075~1100℃。Wherein, in the step S8, the temperature of the secondary baking body is controlled at 1075-1100°C.
其中,将所述S1步骤中,的坯体原料进一步限定为:特级高岭土32~33份、钾长石52~54份、超细石英11~13份、氧化铝粉体6~7份、増白剂3份、増塑剂4份。Wherein, the green body raw materials in the S1 step are further limited to: 32-33 parts of super kaolin, 52-54 parts of potassium feldspar, 11-13 parts of ultrafine quartz, 6-7 parts of alumina powder, 3 parts of whitening agents, 4 parts of plasticizers.
其中,所述氧化铝粉体添加量进一步限定为占坯体原料总质量的6%。Wherein, the addition amount of the alumina powder is further limited to 6% of the total mass of the green body raw materials.
实验一:experiment one:
为了保障产品散热性能,在其余条件不变的情况下,更改原料中氧化铝粉体的占比,进行生产,生产后进行散热测试,记录单位时间内灯罩表面温度下降度数,得到以下数据:In order to ensure the heat dissipation performance of the product, under the condition that other conditions remain unchanged, the proportion of alumina powder in the raw material is changed, and the production is carried out. After production, the heat dissipation test is carried out, and the temperature drop of the lampshade surface per unit time is recorded, and the following data are obtained:
由上可知,当氧化铝粉体添加比占原料总比例的6~6.5%时,陶瓷灯的散热能力优秀,而氧化铝粉体添加比为6%时,陶瓷灯的散热能力最佳,因此,氧化铝粉体添加比优选为6%。It can be seen from the above that when the addition ratio of alumina powder accounts for 6-6.5% of the total proportion of raw materials, the heat dissipation ability of the ceramic lamp is excellent, and when the addition ratio of alumina powder is 6%, the heat dissipation ability of the ceramic lamp is the best, so , the addition ratio of alumina powder is preferably 6%.
以上所述,仅为本发明较佳的具体实施方式,但本发明的保护范围并不局限于此,任何熟悉本技术领域的技术人员在本发明揭露的技术范围内,根据本发明的技术方案及其发明构思加以等同替换或改变,都应涵盖在本发明的保护范围之内。The above is only a preferred embodiment of the present invention, but the scope of protection of the present invention is not limited thereto, any person familiar with the technical field within the technical scope disclosed in the present invention, according to the technical solution of the present invention Any equivalent replacement or change of the inventive concepts thereof shall fall within the protection scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011449611.6A CN115635572B (en) | 2020-12-09 | 2020-12-09 | Lamp forming equipment |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011449611.6A CN115635572B (en) | 2020-12-09 | 2020-12-09 | Lamp forming equipment |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115635572A true CN115635572A (en) | 2023-01-24 |
| CN115635572B CN115635572B (en) | 2025-09-16 |
Family
ID=84939436
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202011449611.6A Active CN115635572B (en) | 2020-12-09 | 2020-12-09 | Lamp forming equipment |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115635572B (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119217514A (en) * | 2024-11-29 | 2024-12-31 | 巢湖学院 | A device and method for automatically positioning and fine-tuning the outer contour of a disc-shaped suspension porcelain insulator |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20010066974A (en) * | 2000-08-10 | 2001-07-12 | 지정철 | A street lamp pole manufacture device and manufacture method |
| CN204819855U (en) * | 2015-07-16 | 2015-12-02 | 玉溪诺德软件开发有限公司 | Computer -aided pottery 3D does not have mould former |
| CN106024226A (en) * | 2016-07-05 | 2016-10-12 | 苏州达力客自动化科技有限公司 | Preceding jiggering device for porcelain insulator |
| CN108942494A (en) * | 2018-08-01 | 2018-12-07 | 邓俊兴 | A kind of Ceramic manufacturing moulded pottery not yet put in a kiln to bake grinding device |
| CN111215371A (en) * | 2020-01-14 | 2020-06-02 | 赣州南牌照明科技有限公司 | Dust removal equipment for LED lamp |
-
2020
- 2020-12-09 CN CN202011449611.6A patent/CN115635572B/en active Active
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20010066974A (en) * | 2000-08-10 | 2001-07-12 | 지정철 | A street lamp pole manufacture device and manufacture method |
| CN204819855U (en) * | 2015-07-16 | 2015-12-02 | 玉溪诺德软件开发有限公司 | Computer -aided pottery 3D does not have mould former |
| CN106024226A (en) * | 2016-07-05 | 2016-10-12 | 苏州达力客自动化科技有限公司 | Preceding jiggering device for porcelain insulator |
| CN108942494A (en) * | 2018-08-01 | 2018-12-07 | 邓俊兴 | A kind of Ceramic manufacturing moulded pottery not yet put in a kiln to bake grinding device |
| CN111215371A (en) * | 2020-01-14 | 2020-06-02 | 赣州南牌照明科技有限公司 | Dust removal equipment for LED lamp |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119217514A (en) * | 2024-11-29 | 2024-12-31 | 巢湖学院 | A device and method for automatically positioning and fine-tuning the outer contour of a disc-shaped suspension porcelain insulator |
| CN119217514B (en) * | 2024-11-29 | 2025-02-25 | 巢湖学院 | Automatic positioning and finishing device and method for outer contour of disc-shaped suspension porcelain insulator |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115635572B (en) | 2025-09-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN210150952U (en) | A device for bending and forming cover glass | |
| CN115534064A (en) | Fire-fighting evacuation ceramic lamp forming process and equipment thereof | |
| CN107495791A (en) | A kind of teacup rack | |
| CN115635572B (en) | Lamp forming equipment | |
| CN114074372B (en) | A kind of fire light technology | |
| CN211492955U (en) | Tablet production is with tablet press of being convenient for clear up powder | |
| CN219049929U (en) | Detachable anti-blocking disposable nasal oxygen cannula | |
| CN210879133U (en) | Polishing equipment for architectural decoration engineering | |
| CN210276009U (en) | A fully automatic three-dimensional mask manufacturing device | |
| CN207522421U (en) | A kind of glass undercuts the clamping device that uses in processing | |
| CN217372674U (en) | Composite solid wood door processing and forming device | |
| CN217453366U (en) | A polishing device for the manufacture of graphite products | |
| CN213352903U (en) | Gypsum mould apparatus for producing | |
| CN212145718U (en) | Grinder is used in controllable mica sheet production of pressure | |
| CN214238750U (en) | Glaze material clearing device | |
| CN213905122U (en) | A suction device for silicon steel sheet mold products | |
| CN211334523U (en) | Full-automatic multi-station positive and negative pressure thermoforming machine | |
| CN208308684U (en) | A kind of circular glass cutting means | |
| CN220813013U (en) | Mask production secondary flattening mechanism | |
| CN219271185U (en) | A fixed denture all-ceramic crown inner crown corrector | |
| CN213918386U (en) | A cutting device for car mat production | |
| CN218928122U (en) | High-precision blank pulling machine for ceramics | |
| CN208250660U (en) | A kind of high-precision hobboing cutter abrasive cutoff machine with positioning function | |
| CN219837979U (en) | Mud training device for ceramic processing | |
| CN221697947U (en) | A heat sealing machine for mask production and processing |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| DD01 | Delivery of document by public notice |
Addressee: Ning Huizhu Document name: Deemed not to have provided notice |
|
| DD01 | Delivery of document by public notice | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address |
Address after: 124000 Liaoning Province Panjin City Liao Dong Bay New District Sag Business and Residential Service Center Building 4 Room 218-284 Patentee after: Suaeda salsa xianchuang Technology (Panjin) Co.,Ltd. Country or region after: China Address before: 124000 Room 203, 2nd floor, science and technology incubator, high tech Industrial Development Zone, 30 Xingye street, Xinglongtai District, Panjin City, Liaoning Province Patentee before: LIAONING HONGXIN TECHNOLOGY ACHIEVEMENT TRANSFORMATION SERVICE CO.,LTD. Country or region before: China |
|
| CP03 | Change of name, title or address |