CN115606609A - A special processing system for whole dry noodles with miscellaneous grains - Google Patents
A special processing system for whole dry noodles with miscellaneous grains Download PDFInfo
- Publication number
- CN115606609A CN115606609A CN202211403948.2A CN202211403948A CN115606609A CN 115606609 A CN115606609 A CN 115606609A CN 202211403948 A CN202211403948 A CN 202211403948A CN 115606609 A CN115606609 A CN 115606609A
- Authority
- CN
- China
- Prior art keywords
- noodle
- dough
- cutting
- forming
- belt
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 235000012149 noodles Nutrition 0.000 title claims abstract description 187
- 230000007246 mechanism Effects 0.000 claims abstract description 195
- 238000005520 cutting process Methods 0.000 claims abstract description 130
- 238000005096 rolling process Methods 0.000 claims abstract description 44
- 230000005540 biological transmission Effects 0.000 claims abstract description 37
- 235000013339 cereals Nutrition 0.000 claims abstract description 35
- 238000001035 drying Methods 0.000 claims abstract description 14
- 210000001161 mammalian embryo Anatomy 0.000 claims abstract description 13
- 235000013305 food Nutrition 0.000 claims abstract 10
- 238000007493 shaping process Methods 0.000 claims abstract 9
- 238000003825 pressing Methods 0.000 claims description 34
- 239000000725 suspension Substances 0.000 claims description 23
- 230000001681 protective effect Effects 0.000 claims description 13
- 230000000694 effects Effects 0.000 claims description 11
- 230000008878 coupling Effects 0.000 claims description 10
- 238000010168 coupling process Methods 0.000 claims description 10
- 238000005859 coupling reaction Methods 0.000 claims description 10
- 230000032258 transport Effects 0.000 claims description 3
- 238000009795 derivation Methods 0.000 claims 1
- 238000007599 discharging Methods 0.000 claims 1
- 238000001125 extrusion Methods 0.000 abstract description 6
- 238000011144 upstream manufacturing Methods 0.000 abstract description 4
- 238000012858 packaging process Methods 0.000 abstract description 3
- 238000004519 manufacturing process Methods 0.000 abstract description 2
- 230000000181 anti-adherent effect Effects 0.000 description 16
- 238000000034 method Methods 0.000 description 13
- 210000002257 embryonic structure Anatomy 0.000 description 12
- 230000008569 process Effects 0.000 description 12
- 238000007790 scraping Methods 0.000 description 9
- 239000000463 material Substances 0.000 description 8
- 238000000465 moulding Methods 0.000 description 8
- 238000010586 diagram Methods 0.000 description 4
- 235000013312 flour Nutrition 0.000 description 4
- 230000009471 action Effects 0.000 description 3
- 230000017105 transposition Effects 0.000 description 3
- 230000008859 change Effects 0.000 description 2
- 239000011248 coating agent Substances 0.000 description 2
- 238000000576 coating method Methods 0.000 description 2
- 238000009434 installation Methods 0.000 description 2
- 238000002156 mixing Methods 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000004806 packaging method and process Methods 0.000 description 2
- 238000000926 separation method Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 230000002452 interceptive effect Effects 0.000 description 1
- 238000004898 kneading Methods 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 230000004060 metabolic process Effects 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 230000001737 promoting effect Effects 0.000 description 1
- 238000003756 stirring Methods 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
Images



Classifications
-
- A—HUMAN NECESSITIES
- A21—BAKING; EDIBLE DOUGHS
- A21C—MACHINES OR EQUIPMENT FOR MAKING OR PROCESSING DOUGHS; HANDLING BAKED ARTICLES MADE FROM DOUGH
- A21C11/00—Other machines for forming the dough into its final shape before cooking or baking
- A21C11/10—Other machines for forming the dough into its final shape before cooking or baking combined with cutting apparatus
-
- A—HUMAN NECESSITIES
- A21—BAKING; EDIBLE DOUGHS
- A21C—MACHINES OR EQUIPMENT FOR MAKING OR PROCESSING DOUGHS; HANDLING BAKED ARTICLES MADE FROM DOUGH
- A21C3/00—Machines or apparatus for shaping batches of dough before subdivision
- A21C3/02—Dough-sheeters; Rolling-machines; Rolling-pins
-
- A—HUMAN NECESSITIES
- A21—BAKING; EDIBLE DOUGHS
- A21C—MACHINES OR EQUIPMENT FOR MAKING OR PROCESSING DOUGHS; HANDLING BAKED ARTICLES MADE FROM DOUGH
- A21C3/00—Machines or apparatus for shaping batches of dough before subdivision
- A21C3/04—Dough-extruding machines ; Hoppers with moving elements, e.g. rollers or belts as wall elements for drawing the dough
-
- A—HUMAN NECESSITIES
- A21—BAKING; EDIBLE DOUGHS
- A21C—MACHINES OR EQUIPMENT FOR MAKING OR PROCESSING DOUGHS; HANDLING BAKED ARTICLES MADE FROM DOUGH
- A21C9/00—Other apparatus for handling dough or dough pieces
- A21C9/08—Depositing, arranging and conveying apparatus for handling pieces, e.g. sheets of dough
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Food Science & Technology (AREA)
- Manufacturing And Processing Devices For Dough (AREA)
Abstract
Description
技术领域technical field
本发明涉及全干宽面条生产技术领域,特别涉及一种能够针对挤出后的面条实现快速辊压切条的全干宽面加工设备,尤其是一种杂粮全干面条食品专用加工系统。The invention relates to the technical field of dry wide noodles production, in particular to a whole dry wide noodle processing equipment capable of quickly rolling and cutting extruded noodles, especially a special processing system for whole dry noodles with miscellaneous grains.
背景技术Background technique
杂粮粗粮面条不仅能够达到促进新陈代谢的作用,还不会有特别高脂肪和热量的情况,深受养生的人群喜爱,目前在市面上也有着大量的杂粮面条品类。Coarse grain noodles can not only achieve the effect of promoting metabolism, but also will not be particularly high in fat and calories. They are very popular among health-preserving people. There are also a large number of miscellaneous grain noodles on the market.
目前市面上的包装好的杂粮全干面条其成型后一般为细长柱状的面条,主要是由面条成型机挤出成型制成,而且目前市面上的面条成型设备一般分为两类。The packaged miscellaneous grain whole dry noodles on the market are generally slender and columnar noodles after being molded, and are mainly extruded and formed by a noodle forming machine, and the noodle forming equipment on the market is generally divided into two types.
第一类为纯手动器械,例如在专利申请号为CN201610202371.7的专利文献中就公开了一种手动挤出成型面条机,其主要结构包括由上、下盖、缸筒连接成的机体内安装连接有摇手柄的传动机构,其特征在于所述传动机构由上端的滚珠丝杆螺母副和下端滚珠丝杆末端连接的推力轴承组件构成,并且所述推力轴承组件与活塞连接成整体,所述活塞与缸筒间隙配合,所述上盖上固定有固定机构,所述固定机构由固定在灶具对面墙立面的支撑环,所述支撑环与支撑杆的一端连接,所述支撑杆的另一端固定在上盖上构成。The first type is a purely manual instrument. For example, a manual extrusion molding noodle machine is disclosed in the patent application number CN201610202371.7. A transmission mechanism connected with a rocker handle is installed, and the transmission mechanism is characterized in that the transmission mechanism is composed of a ball screw nut pair at the upper end and a thrust bearing assembly connected to the end of the ball screw at the lower end, and the thrust bearing assembly is connected with the piston as a whole. The piston and the cylinder are in clearance fit, and a fixing mechanism is fixed on the upper cover. The fixing mechanism consists of a support ring fixed on the opposite wall of the cooker, and the support ring is connected with one end of the support rod. The other end is fixed on the upper cover to form.
第二类为自动化器械,例如在专利申请号为CN201810875706.0的专利文献中就公开了一种全自动面条机,其主要结构包括机壳、和面装置和成型装置;所述机壳为中空结构,其顶部设有进料口;所述和面装置可转动的处于所述机壳内的一侧用于先将面粉搅拌均匀,所述成型装置处于所述机壳的另外一侧用于将搅拌均匀的面粉挤压成型;在所述机壳内设有在面粉搅拌时将所述成型装置处的面粉推向所述和面装置的坡面,所述坡面处于所述机壳内底部的一侧且对应所述成型装置下方的位置处。The second category is automatic equipment. For example, a fully automatic noodle machine is disclosed in the patent application number CN201810875706.0. Its main structure includes a casing, a dough mixing device and a forming device; the casing is hollow structure, the top of which is provided with a feeding port; the rotatable side of the kneading device in the casing is used to stir the flour evenly, and the molding device is located on the other side of the casing for Extrude the evenly stirred flour into shape; when the flour is stirred, there is a slope that pushes the flour at the forming device to the dough mixing device, and the slope is in the casing One side of the bottom corresponds to the position below the molding device.
由上述两类现有技术中的面条机结构可以看出其一般只是针对传统的细长柱状的面条进行加工成型,但是目前由于人们对手工类的手擀面的喜爱程度不断增加,很多时候人们更喜爱手擀面类的宽面面条,而现有的面条成型机并无法有效地、快速地完成宽面全干面条的制备。It can be seen from the noodle machine structures in the above two types of prior art that it generally only processes and shapes traditional elongated columnar noodles. I prefer the wide noodles of hand-rolled noodles, but the existing noodle forming machine can't effectively and quickly complete the preparation of wide dry noodles.
为此,本发明在此提出了一种能够针对挤出后的面条实现快速辊压切条的全干宽面加工设备,用以更好地解决现有技术中存在的问题。For this reason, the present invention proposes a full-dry wide noodle processing equipment that can realize fast rolling and cutting for extruded noodles, so as to better solve the problems existing in the prior art.
发明内容Contents of the invention
本发明为解决上述技术问题之一,所采用的技术方案是:一种杂粮全干面条食品专用加工系统,包括杂粮面团投料机构、面团成型输出机构、动力传动机构,所述面团成型输出机构的底部固定安装在一机架的顶部,所述杂粮面团投料机构安装在所述面团成型输出机构的进料口处,所述动力传动机构安装在所述机架上且用于驱动所述面团成型输出机构运转,在所述面团成型输出机构的出料口下游安装有一皮带送料机构,所述皮带送料机构用于带动由所述面团成型输出机构成型后输出的面条胚向下游运输,在所述皮带送料机构的上方自上游至下游依次设置有若干个固定在悬挂架顶部的面胚辊压机构、面条切料机构、面条烘干室。In order to solve one of the above technical problems, the technical solution adopted by the present invention is: a special processing system for whole dry noodles with miscellaneous grains, including a dough feeding mechanism for miscellaneous grains, a dough forming output mechanism, and a power transmission mechanism. The bottom is fixedly installed on the top of a frame, the multigrain dough feeding mechanism is installed at the feed inlet of the dough forming output mechanism, and the power transmission mechanism is installed on the frame and used to drive the dough forming The output mechanism operates, and a belt feeding mechanism is installed downstream of the discharge port of the dough forming output mechanism, and the belt feeding mechanism is used to drive the noodle embryos outputted by the dough forming output mechanism to be transported downstream. The top of the belt feeding mechanism is sequentially provided with several dough rolling mechanisms, noodle cutting mechanisms and noodle drying chambers fixed on the top of the suspension frame from upstream to downstream.
在上述任一方案中优选的是,所述杂粮面团投料机构包括一面团进料仓,所述面团进料仓的底部出料口连接所述面团成型输出机构的顶部进料口。In any of the above schemes, preferably, the multigrain dough feeding mechanism includes a dough feeding bin, and the bottom outlet of the dough feeding bin is connected to the top feeding port of the dough forming output mechanism.
在上述任一方案中优选的是,所述面团成型输出机构包括固定安装在所述机架顶部的卧式螺旋成型机,所述卧式螺旋成型机的右端出料口处连接有一用于将条状面胚向外输送的导出弯管,所述导出弯管的末端位于所述皮带送料机构的上方,在所述卧式螺旋成型机的内腔内安装有螺旋输料轴,所述螺旋输料轴的左端向左活动穿出所述卧式螺旋成型机的左端盖后并通过联轴器与所述动力传动机构的输出端相连接。In any of the above schemes, it is preferred that the dough forming output mechanism includes a horizontal screw forming machine fixedly installed on the top of the frame, and the right end outlet of the horizontal screw forming machine is connected with a The outlet elbow for conveying strip-shaped dough outwards, the end of the outlet elbow is located above the belt feeding mechanism, and a screw feeding shaft is installed in the inner cavity of the horizontal screw forming machine. The left end of the feeding shaft passes through the left end cover of the horizontal screw forming machine to the left and is connected with the output end of the power transmission mechanism through a coupling.
在上述任一方案中优选的是,所述动力传动机构包括固定安装在所述机架上的成型驱动电机,在所述成型驱动电机的电机轴端固定安装有一成型驱动带轮,在所述成型驱动带轮的左侧的机架处活动铰接有一成型从动带轮,所述成型从动带轮与所述成型驱动带轮之间通过成型传动皮带相连接,在所述成型从动带轮的中心轴的内端连接有一换向机构,所述换向机构的输出端通过联轴器与所述螺旋输料轴的左端相连接。In any of the above schemes, it is preferred that the power transmission mechanism includes a forming drive motor fixedly installed on the frame, and a forming drive pulley is fixedly installed on the motor shaft end of the forming drive motor. A molding driven pulley is hinged at the frame on the left side of the molding drive pulley, and the molding driven pulley is connected to the molding driving pulley through a molding transmission belt. The inner end of the center shaft of the wheel is connected with a reversing mechanism, and the output end of the reversing mechanism is connected with the left end of the screw feeding shaft through a coupling.
在上述任一方案中优选的是,所述换向机构包括一固定安装在所述机架上的齿轮箱,在所述齿轮箱的底部安装有一底部锥齿轮,所述底部锥齿轮的齿轮轴水平向外活动穿出所述齿轮箱后并与所述成型从动带轮的中心轴固连,在所述底部锥齿轮的右侧啮合有一换向锥齿轮,在所述换向锥齿轮的锥齿轮轴的右侧固连有一换向直齿轮,在所述换向直齿轮的上方啮合有一传动直齿轮,所述传动直齿轮的直齿轮轴右端活动穿出所述齿轮箱并通过联轴器与所述螺旋输料轴相连接。In any of the above schemes, preferably, the reversing mechanism includes a gear box fixedly installed on the frame, a bottom bevel gear is installed at the bottom of the gear box, and the gear shaft of the bottom bevel gear After passing through the gear box horizontally outwards and fixedly connected with the central shaft of the formed driven pulley, a reversing bevel gear is meshed on the right side of the bottom bevel gear. A reversing spur gear is fixedly connected to the right side of the bevel gear shaft, and a transmission spur gear is meshed above the reversing spur gear. The right end of the spur gear shaft of the transmission spur gear moves out of the gearbox and passes through the coupling. The device is connected with the screw feeding shaft.
在上述任一方案中优选的是,所述皮带送料机构包括一皮带输送机,在所述皮带输送机的上层和下层的输送皮带的底部沿其输送方向均间隔安装有若干个定轴旋转的支撑托辊,所述输送皮带的两端分别安装有驱动输送皮带轮、从动输送皮带轮,所述驱动输送皮带轮由外部的驱动输送电机实现驱动。In any of the above schemes, it is preferred that the belt feeding mechanism includes a belt conveyor, and several fixed-axis rotating conveyor belts are installed at intervals along the conveying direction at the bottom of the upper and lower conveyor belts of the belt conveyor. Support rollers, the two ends of the conveying belt are respectively equipped with a driving conveying pulley and a driven conveying pulley, and the driving conveying pulley is driven by an external driving conveying motor.
在上述任一方案中优选的是,所述面胚辊压机构包括两分别沿输送皮带的宽度方向间隔设置且顶部固定在所述悬挂架的底部的辊压调位缸,两所述辊压调位缸同步运动,在两所述辊压调位缸的活塞杆的底部分别固连有一辊压轴承座,在两所述辊压轴承座之间活动安装有一面胚压辊,所述面胚压辊的底部用于抵接压紧输送过来的条状面胚并将其压制成薄片状继续向前输送。In any of the above schemes, it is preferred that the dough rolling mechanism includes two roller pressure adjustment cylinders which are respectively arranged at intervals along the width direction of the conveying belt and whose top is fixed on the bottom of the suspension frame. The positioning cylinders move synchronously. A rolling bearing seat is fixedly connected to the bottoms of the piston rods of the two rolling positioning cylinders, and a blank pressing roller is installed between the two rolling bearing seats. The bottom of the embryo pressing roller is used to abut against the strip-shaped dough embryo that is conveyed by pressing and compressing it into a thin sheet to continue forward conveying.
在上述任一方案中优选的是,在所述输送皮带的两侧顶部均固定安装有防护挡板。In any of the above schemes, it is preferred that protective baffles are fixedly installed on the tops of both sides of the conveyor belt.
在上述任一方案中优选的是,所述面条切料机构用于实现将被辊压成薄片状的面胚切割成若干条的宽面条;In any of the above schemes, it is preferred that the noodle cutting mechanism is used to cut the rolled dough into thin sheets into several wide noodles;
所述面条切料机构包括两分别沿输送皮带的宽度方向间隔设置且顶部固定在所述悬挂架的底部的切面控制缸,两所述切面控制缸为同步运动,在两所述切面控制缸的活塞杆的底部均固连有一切面轴承座,两所述切面轴承座之间活动铰接有一切面辊轮,所述切面辊轮通过与其中心固连的切面转动轴活动穿出对应位置处的所述切面轴承座,所述切面转动轴的一端与一刀位调位单元相连接,在所述切面辊轮的上部和下部的外侧壁上沿输送皮带的宽度方向依次间隔安装有若干个切面刀具,位于下部的各所述切面刀具用于跟随两所述切面控制缸的升降来实现对由输送皮带送过来的薄状面胚实现快切分隔成多条宽面条。The noodle cutting mechanism includes two cutting surface control cylinders arranged at intervals along the width direction of the conveyor belt and the top is fixed on the bottom of the suspension frame. The two cutting surface control cylinders move synchronously. The bottom of the piston rod is fixedly connected with a tangential bearing seat, and a tangential roller is articulated between the two tangential bearing pedestals, and the tangential roller moves out of the corresponding position through the tangential rotating shaft fixed to the center. In the section bearing seat, one end of the section rotation shaft is connected to a knife position adjustment unit, and several section section knives are installed at intervals along the width direction of the conveyor belt on the upper and lower outer sidewalls of the section section roller. Each of the noodle-cut knives positioned at the lower part is used to follow the lifting of the two noodle-cut control cylinders to realize fast cutting and separation of the thin noodle embryos sent by the conveyor belt into a plurality of lasagna noodles.
在上述任一方案中优选的是,在下部的各所述切面刀具的底部安装有一压面防粘机构,所述压面防粘机构包括一防粘压面薄板,所述防粘压面薄板的两端向上翘起且呈水平吊挂部,在所述防粘压面薄板的底部沿其宽度方向依次间隔设置有若干个分别位于对应的切面刀具底部的刮面长槽,各所述刮面长槽沿所述面条的输送方向设置且不会对上部和下部的切面刀具的换位造成干涉,当个切面刀具由对应的刮面长槽穿过时可以将切面刀具两侧粘连的面胚刮除。In any of the above schemes, it is preferred that a pressing surface anti-sticking mechanism is installed at the bottom of each of the lower cutting tools, and the pressing surface anti-sticking mechanism includes an anti-sticking pressing surface thin plate, and the anti-sticking pressing surface thin plate The two ends of the anti-adhesive pressing surface are tilted upwards and form a horizontal hanging part. On the bottom of the anti-adhesive pressing surface sheet, there are several long scraping grooves respectively located at the bottom of the corresponding cutting cutter at intervals along its width direction. The noodle length grooves are arranged along the conveying direction of the noodles without interfering with the transposition of the upper and lower noodle cutters. When a noodle cutter passes through the corresponding scraping noodle long grooves, the noodle embryos adhered on both sides of the noodle cutters can be scrape off.
在上述任一方案中优选的是,所述防粘压面薄板的两所述水平吊挂部的顶部分别固定在一立柱,两所述立柱的顶部均活动伸至所述悬挂架的上方,在各所述立柱的外侧壁上分别套接有一吊挂弹簧,两所述吊挂弹簧的顶部分别固定在所述悬挂架的底部,两所述吊挂弹簧的底部均固定在对应位置处的所述水平吊挂部的顶部。In any of the above schemes, it is preferred that the tops of the two horizontal hanging parts of the anti-adhesive pressure surface thin plate are respectively fixed on a column, and the tops of the two columns are all movably extended above the suspension frame, A suspension spring is respectively sleeved on the outer side wall of each of the columns, the tops of the two suspension springs are respectively fixed on the bottom of the suspension frame, and the bottoms of the two suspension springs are fixed at the corresponding positions. the top of the horizontal hanging part.
在上述任一方案中优选的是,所述刀位调位单元包括固定安装在对应位置处的所述切面控制缸的活塞杆的一侧的刀具调位电机,所述刀具调位电机的电机轴与所述切面转动轴的端部固连,所述刀具调位电机通过旋转带动所述切面辊轮的旋转,从而达到带动上部的各所述切面刀具各下部的各所述切面刀具旋转换位的目的。In any of the above schemes, preferably, the tool position adjustment unit includes a tool position adjustment motor fixedly installed on one side of the piston rod of the cutting surface control cylinder at the corresponding position, and the motor of the tool position adjustment motor The shaft is fixedly connected with the end of the cutting surface rotating shaft, and the cutter positioning motor drives the rotation of the cutting surface rollers through rotation, so as to drive each of the cutting surface cutters on the upper part and each of the cutting surface cutters on the lower part to rotate. bit purpose.
在所述导出弯管的出料口处还设置有一面胚截断机构,所述面胚截断机构包括固定安装在所述悬挂架底部的截断控制缸,在所述截断控制缸的活塞杆的底部固定安装有一截断电机,所述截断电机的电机轴处连接有一旋转截断刀盘,所述旋转截断刀盘的底部通过旋转将由导出弯管的出料口处挤出的面胚实现按需截断。A face blank cutting mechanism is also provided at the discharge port of the lead-out elbow, and the dough cutting mechanism includes a cutting control cylinder fixedly installed at the bottom of the suspension frame, and at the bottom of the piston rod of the cutting control cylinder A cut-off motor is fixedly installed, and the motor shaft of the cut-off motor is connected with a rotary cut-off cutterhead, and the bottom of the rotary cut-off cutterhead is cut off on demand by rotating the dough extruded from the outlet of the leading elbow.
在所述导出弯管的出料口处的下方还固定安装有一防护导料板,所述防护导料板位于所述旋转截断刀盘下方且与其间隔设置。A protective material guide plate is also fixedly installed below the discharge port of the lead-out elbow, and the protective material guide plate is located below the rotary cutting cutter head and is spaced apart from it.
与现有技术相比,本发明的有益效果如下:Compared with the prior art, the beneficial effects of the present invention are as follows:
1、本系统能够对杂粮面团、面胚进行挤压成型,同时成型后可以实现对面胚的快速辊压成面,然后切割成鲜宽面条,最终由烘干室可以实现对宽面条的烘干成型,便于送入后续包装工序。1. This system can extrude and shape miscellaneous grain dough and dough embryo. At the same time, after forming, the dough embryo can be quickly rolled into noodles, and then cut into fresh wide noodles. Finally, the drying room can realize the drying of wide noodles Molded, easy to send into the subsequent packaging process.
2、本系统中在利用面团成型输出机构进行输送时能够有效地依靠动力传动机构上的换向机构实现对面胚的快速螺旋输送、挤压成型后导出,保证向外挤出条状面胚的速度。2. In this system, when the dough forming output mechanism is used for conveying, it can effectively rely on the reversing mechanism on the power transmission mechanism to realize the rapid spiral conveying of the opposite dough, and export it after extrusion, so as to ensure the extrusion of the strip-shaped dough. speed.
3、本系统中利用面胚辊压机构可以将输送状态下的条状面胚快速的辊压成薄片状的面片,等待后续的面条切料机构可以将其快速分切成若干条的宽面条,从而可以实现类似于人工制成的手擀宽面面条。3. In this system, the dough rolling mechanism can be used to quickly roll the strip-shaped dough in the conveying state into a thin sheet of dough, and wait for the subsequent noodle cutting mechanism to quickly cut it into several strips of width. Noodles, thus making it possible to achieve lasagna noodles similar to those made by hand.
4、在利用面条切料机构进行面条的分切的过程中本系统中还设计了压面防粘机构实现在切面的过程中防止面条被粘起,同时还能够有效地对已经站在各切面刀具上的面块实现刮料脱料,从而保证切面工序的切面效果。4. In the process of cutting noodles by using the noodle cutting mechanism, this system is also designed with a pressure surface anti-sticking mechanism to prevent the noodles from being stuck during the cutting process, and at the same time, it can effectively clean the noodles that have already stood on each cutting surface. The noodle block on the cutter realizes scraping and stripping, so as to ensure the cutting effect of the noodle cutting process.
5、本系统中增设的面胚截断机构可以根据设定需要的面条的长度进行周期性的将导出的面胚进行截断,保证面条的长度符合要求,同时在截断面条的过程中利用防护导料板可以起到防止截断刀盘直接接触输送皮带的目的,更好地起到防护作用。5. The noodle cutting mechanism added in this system can periodically cut off the exported noodle according to the length of the required noodles to ensure that the length of the noodle meets the requirements. At the same time, the protection guide is used in the process of cutting the noodles The plate can prevent the cut-off cutter head from directly contacting the conveying belt, and better protect it.
附图说明Description of drawings
为了更清楚地说明本发明具体实施方式或现有技术中的技术方案,下面将对具体实施方式或现有技术描述中所需要使用的附图作简单地介绍。在所有附图中,类似的元件或部件一般由类似的附图标记标识。附图中,各元件或部件并不一定按照实际的比例绘制。In order to more clearly illustrate the specific embodiments of the present invention or the technical solutions in the prior art, the following will briefly introduce the drawings that need to be used in the description of the specific embodiments or the prior art. Throughout the drawings, similar elements or components are generally identified by similar reference numerals. In the drawings, elements or parts are not necessarily drawn in actual scale.
图1为本发明的结构示意图。Fig. 1 is a structural schematic diagram of the present invention.
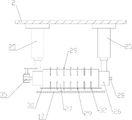
图2为本发明的面条切料机构的局部放大结构示意图。Fig. 2 is a partial enlarged structural schematic diagram of the noodle cutting mechanism of the present invention.
图3为图2中的面条切料机构的侧视局部结构示意图。Fig. 3 is a side view partial structural schematic diagram of the noodle cutting mechanism in Fig. 2 .
图4为本发明的换向机构的内部结构示意图。Fig. 4 is a schematic diagram of the internal structure of the reversing mechanism of the present invention.
图中,1、机架;2、悬挂架;3、面条烘干室;4、面团进料仓;5、卧式螺旋成型机;6、导出弯管;7、螺旋输料轴;8、联轴器;9、齿轮箱;10、底部锥齿轮;11、成型从动带轮;12、换向锥齿轮;13、换向直齿轮;14、传动直齿轮;15、直齿轮轴;16、皮带输送机;17、输送皮带;18、支撑托辊;19、驱动输送皮带轮;20、从动输送皮带轮;21、辊压调位缸;22、辊压轴承座;23、面胚压辊;24、防护挡板;25、切面控制缸;26、切面轴承座;27、切面辊轮;28、切面转动轴;29、切面刀具;30、防粘压面薄板;31、水平吊挂部;32、刮面长槽;33、立柱;34、吊挂弹簧;35、刀具调位电机;36、截断控制缸;37、截断电机;38、旋转截断刀盘;39、防护导料板。In the figure, 1. Rack; 2. Suspension frame; 3. Noodle drying chamber; 4. Dough feeding bin; 5. Horizontal screw forming machine; Coupling; 9. Gear box; 10. Bottom bevel gear; 11. Formed driven pulley; 12. Reversing bevel gear; 13. Reversing spur gear; 14. Transmission spur gear; 15. Spur gear shaft; 16 , belt conveyor; 17, conveying belt; 18, support roller; 19, driving conveying pulley; 20, driven conveying pulley; 21, roller pressure adjustment cylinder; 22, roller bearing seat; 23,
具体实施方式detailed description
下面将结合附图对本发明技术方案的实施例进行详细的描述。以下实施例仅用于更加清楚地说明本发明的技术方案,因此只作为示例,而不能以此来限制本发明的保护范围。本发明具体结构如图1-4中所示。Embodiments of the technical solutions of the present invention will be described in detail below in conjunction with the accompanying drawings. The following examples are only used to illustrate the technical solutions of the present invention more clearly, and therefore are only examples, rather than limiting the protection scope of the present invention. The specific structure of the present invention is shown in Fig. 1-4.
实施例1:Example 1:
一种杂粮全干面条食品专用加工系统,包括杂粮面团投料机构、面团成型输出机构、动力传动机构,所述面团成型输出机构的底部固定安装在一机架1的顶部,所述杂粮面团投料机构安装在所述面团成型输出机构的进料口处,所述动力传动机构安装在所述机架1上且用于驱动所述面团成型输出机构运转,在所述面团成型输出机构的出料口下游安装有一皮带送料机构,所述皮带送料机构用于带动由所述面团成型输出机构成型后输出的面条胚向下游运输,在所述皮带送料机构的上方自上游至下游依次设置有若干个固定在悬挂架2顶部的面胚辊压机构、面条切料机构、面条烘干室3。本系统在进行工作时先将电源接通,启动整个系统的各零部件以及对应位置处配套设置的到位开关等传感器部件。利用杂粮面团投料机构可以向内部投放粗粮杂粮面团,经过投放的面团会进入到面团成型输出机构,然后由动力传动机构可以控制面团成型输出机构对面胚成型速度的控制,成型的条状面胚会由面团成型输出机构向外输出,然后落入到输送皮带17送料机构,经过面胚辊压机构进行辊压成面片,然后在继续向前输送并经过面条切料机构的快切使其成为若干条的鲜宽面条,各宽鲜面条继续向前输送进入到面条烘干室3内部经过充分的烘干后输送至下游进行包装处理。A special processing system for whole dry noodles with miscellaneous grains, comprising a miscellaneous grains dough feeding mechanism, a dough forming output mechanism, and a power transmission mechanism, the bottom of the dough forming output mechanism is fixedly installed on the top of a frame 1, and the miscellaneous grains dough feeding mechanism Installed at the feed inlet of the dough forming output mechanism, the power transmission mechanism is installed on the frame 1 and used to drive the dough forming output mechanism to run, at the discharge port of the dough forming output mechanism A belt feeding mechanism is installed in the downstream, and the belt feeding mechanism is used to drive the noodle embryos outputted by the dough forming output mechanism to be transported downstream. Above the belt feeding mechanism, a number of fixed rollers are sequentially arranged from upstream to downstream. Dough rolling mechanism, noodle cutting mechanism, noodle drying chamber 3 at the top of
在上述任一方案中优选的是,所述杂粮面团投料机构包括一面团进料仓4,所述面团进料仓4的底部出料口连接所述面团成型输出机构的顶部进料口。In any of the above schemes, preferably, the multigrain dough feeding mechanism includes a dough feeding bin 4, and the bottom outlet of the dough feeding bin 4 is connected to the top feeding port of the dough forming output mechanism.
在上述任一方案中优选的是,所述面团成型输出机构包括固定安装在所述机架1顶部的卧式螺旋成型机5,所述卧式螺旋成型机5的右端出料口处连接有一用于将条状面胚向外输送的导出弯管6,所述导出弯管6的末端位于所述皮带送料机构的上方,在所述卧式螺旋成型机5的内腔内安装有螺旋输料轴7,所述螺旋输料轴7的左端向左活动穿出所述卧式螺旋成型机5的左端盖后并通过联轴器8与所述动力传动机构的输出端相连接。面团成型输出机构工作时,由面团进料仓4送入到卧式螺旋成型机5内部的面团会在运动状态的螺旋输料轴7的作用下不断地向下游输送,最终面胚由右端出料口导出成条状面胚。In any of the above schemes, it is preferred that the dough forming output mechanism includes a horizontal screw forming machine 5 fixedly installed on the top of the frame 1, and a discharge port at the right end of the horizontal screw forming machine 5 is connected to a The outlet elbow 6 for conveying the strip-shaped dough outwards, the end of the outlet elbow 6 is located above the belt feeding mechanism, and a screw conveyor is installed in the inner cavity of the horizontal screw forming machine 5. The material shaft 7, the left end of the screw feeding shaft 7 moves to the left and passes through the left end cover of the horizontal screw forming machine 5 and is connected with the output end of the power transmission mechanism through a coupling 8. When the dough forming output mechanism is working, the dough fed into the horizontal screw forming machine 5 by the dough feeding bin 4 will be continuously conveyed downstream under the action of the moving screw feeding shaft 7, and finally the dough will come out from the right end. The feed port is exported into strip-shaped dough embryos.
在上述任一方案中优选的是,所述动力传动机构包括固定安装在所述机架1上的成型驱动电机,在所述成型驱动电机的电机轴端固定安装有一成型驱动带轮,在所述成型驱动带轮的左侧的机架1处活动铰接有一成型从动带轮11,所述成型从动带轮11与所述成型驱动带轮之间通过成型传动皮带相连接,在所述成型从动带轮11的中心轴的内端连接有一换向机构,所述换向机构的输出端通过联轴器8与所述螺旋输料轴7的左端相连接。在卧式螺旋成型机5的螺旋输料轴7工作的过程中可以通过控制动力传动机构的成型驱动电机的运转速度来调控向外导出面胚的速度,当成型驱动电机工作时会带动成型驱动带轮、成型从动带轮11运转并将动力输送至换向机构,经过换向机构的换向后送至螺旋输料轴7。In any of the above schemes, it is preferred that the power transmission mechanism includes a forming drive motor fixedly installed on the frame 1, and a forming drive pulley is fixedly installed on the motor shaft end of the forming drive motor. The frame 1 on the left side of the forming drive pulley is articulated with a forming driven pulley 11, and the forming driven pulley 11 is connected with the forming driving pulley by a forming transmission belt. The inner end of the center shaft of the forming driven pulley 11 is connected with a reversing mechanism, and the output end of the reversing mechanism is connected with the left end of the screw feeding shaft 7 through a shaft coupling 8 . During the working process of the screw feeding shaft 7 of the horizontal screw forming machine 5, the speed of exporting the dough blank can be adjusted by controlling the running speed of the forming drive motor of the power transmission mechanism. When the forming drive motor is working, it will drive the forming drive. Belt pulley, forming driven pulley 11 run and power is delivered to the reversing mechanism, and sent to the screw feeding shaft 7 after the reversing of the reversing mechanism.
在上述任一方案中优选的是,所述皮带送料机构包括一皮带输送机16,在所述皮带输送机16的上层和下层的输送皮带17的底部沿其输送方向均间隔安装有若干个定轴旋转的支撑托辊18,所述输送皮带17的两端分别安装有驱动输送皮带轮19、从动输送皮带轮20,所述驱动输送皮带轮19由外部的驱动输送电机实现驱动。皮带送料机构在运转时主要是依靠皮带输送机16的运转实现对输送皮带17的驱动,同时设置各个支撑托辊18的目的可以保证输送皮带17的良好支撑性,控制外部的驱动输送电机的输送速度可以控制整个输送皮带17及其上的面胚、面片、宽面条的输送速度。Preferably in any of the above schemes, the belt feeding mechanism includes a belt conveyor 16, and several fixed belts are installed at intervals along the conveying direction at the bottom of the upper and
在上述任一方案中优选的是,所述面胚辊压机构包括两分别沿输送皮带17的宽度方向间隔设置且顶部固定在所述悬挂架2的底部的辊压调位缸21,两所述辊压调位缸21同步运动,在两所述辊压调位缸21的活塞杆的底部分别固连有一辊压轴承座22,在两所述辊压轴承座22之间活动安装有一面胚压辊23,所述面胚压辊23的底部用于抵接压紧输送过来的条状面胚并将其压制成薄片状继续向前输送。面胚辊压机构在此设置为了可以由两个辊压调位缸21带动实现不同高度升降的结构,其可以实现根据不同的要求实现辊压处不同厚度的面片,从而控制后续的宽面条的厚度。在面胚压辊23辊压的过程中可快速的实现对由输送皮带17输送过来的面胚的高效辊压,保证辊压成型的效果。In any of the above schemes, it is preferred that the dough rolling mechanism includes two rolling positioning cylinders 21 that are respectively arranged at intervals along the width direction of the conveying
在上述任一方案中优选的是,所述面条切料机构用于实现将被辊压成薄片状的面胚切割成若干条的宽面条;所述面条切料机构包括两分别沿输送皮带17的宽度方向间隔设置且顶部固定在所述悬挂架2的底部的切面控制缸25,两所述切面控制缸25为同步运动,在两所述切面控制缸25的活塞杆的底部均固连有一切面轴承座26,两所述切面轴承座26之间活动铰接有一切面辊轮27,所述切面辊轮27通过与其中心固连的切面转动轴28活动穿出对应位置处的所述切面轴承座26,所述切面转动轴28的一端与一刀位调位单元相连接,在所述切面辊轮27的上部和下部的外侧壁上沿输送皮带17的宽度方向依次间隔安装有若干个切面刀具29,位于下部的各所述切面刀具29用于跟随两所述切面控制缸25的升降来实现对由输送皮带17送过来的薄状面胚实现快切分隔成多条宽面条。面条切料机构上的两切面控制缸25通过外部控制其按需下降到设定的位置后,可以各个切面刀具29对进入到面条切料机构下方的输送皮带17上的面片进行压切,在压切的过程中薄状面胚被快切分隔成多条宽面条,从而继续向下游输送。当下部的各个切面刀具29使用一段时间且粘接在面块后,可以控制刀位调位单元旋转来将原来处于上部的各个切面刀具29进行调位,然后继续进行切面。控制两个切面控制缸25向下伸出的幅度可以控制切面的深度和效果。In any of the above schemes, it is preferred that the noodle cutting mechanism is used to cut the rolled dough into thin sheets into several wide noodles; The width direction interval is set and the top is fixed on the
实施例2:Example 2:
一种杂粮全干面条食品专用加工系统,包括杂粮面团投料机构、面团成型输出机构、动力传动机构,所述面团成型输出机构的底部固定安装在一机架1的顶部,所述杂粮面团投料机构安装在所述面团成型输出机构的进料口处,所述动力传动机构安装在所述机架1上且用于驱动所述面团成型输出机构运转,在所述面团成型输出机构的出料口下游安装有一皮带送料机构,所述皮带送料机构用于带动由所述面团成型输出机构成型后输出的面条胚向下游运输,在所述皮带送料机构的上方自上游至下游依次设置有若干个固定在悬挂架2顶部的面胚辊压机构、面条切料机构、面条烘干室3。A special processing system for whole dry noodles with miscellaneous grains, comprising a miscellaneous grains dough feeding mechanism, a dough forming output mechanism, and a power transmission mechanism, the bottom of the dough forming output mechanism is fixedly installed on the top of a frame 1, and the miscellaneous grains dough feeding mechanism Installed at the feed inlet of the dough forming output mechanism, the power transmission mechanism is installed on the frame 1 and used to drive the dough forming output mechanism to run, at the discharge port of the dough forming output mechanism A belt feeding mechanism is installed in the downstream, and the belt feeding mechanism is used to drive the noodle embryos outputted by the dough forming output mechanism to be transported downstream. Above the belt feeding mechanism, a number of fixed rollers are sequentially arranged from upstream to downstream. Dough rolling mechanism, noodle cutting mechanism, noodle drying chamber 3 at the top of
在上述任一方案中优选的是,所述杂粮面团投料机构包括一面团进料仓4,所述面团进料仓4的底部出料口连接所述面团成型输出机构的顶部进料口。In any of the above schemes, preferably, the multigrain dough feeding mechanism includes a dough feeding bin 4, and the bottom outlet of the dough feeding bin 4 is connected to the top feeding port of the dough forming output mechanism.
在上述任一方案中优选的是,所述面团成型输出机构包括固定安装在所述机架1顶部的卧式螺旋成型机5,所述卧式螺旋成型机5的右端出料口处连接有一用于将条状面胚向外输送的导出弯管6,所述导出弯管6的末端位于所述皮带送料机构的上方,在所述卧式螺旋成型机5的内腔内安装有螺旋输料轴7,所述螺旋输料轴7的左端向左活动穿出所述卧式螺旋成型机5的左端盖后并通过联轴器8与所述动力传动机构的输出端相连接。In any of the above schemes, it is preferred that the dough forming output mechanism includes a horizontal screw forming machine 5 fixedly installed on the top of the frame 1, and a discharge port at the right end of the horizontal screw forming machine 5 is connected to a The outlet elbow 6 for conveying the strip-shaped dough outwards, the end of the outlet elbow 6 is located above the belt feeding mechanism, and a screw conveyor is installed in the inner cavity of the horizontal screw forming machine 5. The material shaft 7, the left end of the screw feeding shaft 7 moves to the left and passes through the left end cover of the horizontal screw forming machine 5 and is connected with the output end of the power transmission mechanism through a coupling 8.
面团成型输出机构工作时,由面团进料仓4送入到卧式螺旋成型机5内部的面团会在运动状态的螺旋输料轴7的作用下不断地向下游输送,最终面胚由右端出料口导出成条状面胚。When the dough forming output mechanism is working, the dough fed into the horizontal screw forming machine 5 by the dough feeding bin 4 will be continuously conveyed downstream under the action of the moving screw feeding shaft 7, and finally the dough will come out from the right end. The feed port is exported into strip-shaped dough embryos.
在上述任一方案中优选的是,所述动力传动机构包括固定安装在所述机架1上的成型驱动电机,在所述成型驱动电机的电机轴端固定安装有一成型驱动带轮,在所述成型驱动带轮的左侧的机架1处活动铰接有一成型从动带轮11,所述成型从动带轮11与所述成型驱动带轮之间通过成型传动皮带相连接,在所述成型从动带轮11的中心轴的内端连接有一换向机构,所述换向机构的输出端通过联轴器8与所述螺旋输料轴7的左端相连接。In any of the above schemes, it is preferred that the power transmission mechanism includes a forming drive motor fixedly installed on the frame 1, and a forming drive pulley is fixedly installed on the motor shaft end of the forming drive motor. The frame 1 on the left side of the forming drive pulley is articulated with a forming driven pulley 11, and the forming driven pulley 11 is connected with the forming driving pulley by a forming transmission belt. The inner end of the center shaft of the forming driven pulley 11 is connected with a reversing mechanism, and the output end of the reversing mechanism is connected with the left end of the screw feeding shaft 7 through a shaft coupling 8 .
在卧式螺旋成型机5的螺旋输料轴7工作的过程中可以通过控制动力传动机构的成型驱动电机的运转速度来调控向外导出面胚的速度,当成型驱动电机工作时会带动成型驱动带轮、成型从动带轮11运转并将动力输送至换向机构,经过换向机构的换向后送至螺旋输料轴7。During the working process of the screw feeding shaft 7 of the horizontal screw forming machine 5, the speed of exporting the dough blank can be adjusted by controlling the running speed of the forming drive motor of the power transmission mechanism. When the forming drive motor is working, it will drive the forming drive. Belt pulley, forming driven pulley 11 run and power is delivered to the reversing mechanism, and sent to the screw feeding shaft 7 after the reversing of the reversing mechanism.
在上述任一方案中优选的是,所述换向机构包括一固定安装在所述机架1上的齿轮箱9,在所述齿轮箱9的底部安装有一底部锥齿轮10,所述底部锥齿轮10的齿轮轴水平向外活动穿出所述齿轮箱9后并与所述成型从动带轮11的中心轴固连,在所述底部锥齿轮10的右侧啮合有一换向锥齿轮12,在所述换向锥齿轮12的锥齿轮轴的右侧固连有一换向直齿轮13,在所述换向直齿轮13的上方啮合有一传动直齿轮14,所述传动直齿轮14的直齿轮轴15右端活动穿出所述齿轮箱9并通过联轴器8与所述螺旋输料轴7相连接。In any of the above schemes, preferably, the reversing mechanism includes a
在此设置的换向机构中的底部锥齿轮10作为动力输入件,通过底部锥齿轮10与换向锥齿轮12的啮合以及换向直齿轮13与传动直齿轮14的啮合可实现动力的快速切换,保证对螺旋输料轴7的驱动。The
在此增设的换向机构可以更好地实现整个动力驱动件的下沉式安装,降低上部安装的占用空间,同时便于后续拆卸维修。The reversing mechanism added here can better realize the sunken installation of the entire power drive, reduce the space occupied by the upper installation, and facilitate subsequent disassembly and maintenance.
在上述任一方案中优选的是,所述皮带送料机构包括一皮带输送机16,在所述皮带输送机16的上层和下层的输送皮带17的底部沿其输送方向均间隔安装有若干个定轴旋转的支撑托辊18,所述输送皮带17的两端分别安装有驱动输送皮带轮19、从动输送皮带轮20,所述驱动输送皮带轮19由外部的驱动输送电机实现驱动。Preferably in any of the above schemes, the belt feeding mechanism includes a belt conveyor 16, and several fixed belts are installed at intervals along the conveying direction at the bottom of the upper and
皮带送料机构在运转时主要是依靠皮带输送机16的运转实现对输送皮带17的驱动,同时设置各个支撑托辊18的目的可以保证输送皮带17的良好支撑性,控制外部的驱动输送电机的输送速度可以控制整个输送皮带17及其上的面胚、面片、宽面条的输送速度。The belt feeding mechanism mainly relies on the operation of the belt conveyor 16 to drive the
在上述任一方案中优选的是,所述面胚辊压机构包括两分别沿输送皮带17的宽度方向间隔设置且顶部固定在所述悬挂架2的底部的辊压调位缸21,两所述辊压调位缸21同步运动,在两所述辊压调位缸21的活塞杆的底部分别固连有一辊压轴承座22,在两所述辊压轴承座22之间活动安装有一面胚压辊23,所述面胚压辊23的底部用于抵接压紧输送过来的条状面胚并将其压制成薄片状继续向前输送。In any of the above schemes, it is preferred that the dough rolling mechanism includes two rolling positioning cylinders 21 that are respectively arranged at intervals along the width direction of the conveying
面胚辊压机构在此设置为可以由两个辊压调位缸21带动实现不同高度升降的结构,其可以实现根据不同的要求实现辊压处不同厚度的面片,从而控制后续的宽面条的厚度。在面胚压辊23辊压的过程中可快速的实现对由输送皮带17输送过来的面胚的高效辊压,保证辊压成型的效果。The dough rolling mechanism is set here as a structure that can be driven by two rolling position adjustment cylinders 21 to achieve different heights, which can realize different thicknesses of noodles at the rolling position according to different requirements, thereby controlling the subsequent lasagna noodles thickness of. During the rolling process of the
在上述任一方案中优选的是,在所述输送皮带17的两侧顶部均固定安装有防护挡板24。可以有效地起到防护的作用。In any of the above schemes, it is preferable that
在上述任一方案中优选的是,所述面条切料机构用于实现将被辊压成薄片状的面胚切割成若干条的宽面条;In any of the above schemes, it is preferred that the noodle cutting mechanism is used to cut the rolled dough into thin sheets into several wide noodles;
所述面条切料机构包括两分别沿输送皮带17的宽度方向间隔设置且顶部固定在所述悬挂架2的底部的切面控制缸25,两所述切面控制缸25为同步运动,在两所述切面控制缸25的活塞杆的底部均固连有一切面轴承座26,两所述切面轴承座26之间活动铰接有一切面辊轮27,所述切面辊轮27通过与其中心固连的切面转动轴28活动穿出对应位置处的所述切面轴承座26,所述切面转动轴28的一端与一刀位调位单元相连接,在所述切面辊轮27的上部和下部的外侧壁上沿输送皮带17的宽度方向依次间隔安装有若干个切面刀具29,位于下部的各所述切面刀具29用于跟随两所述切面控制缸25的升降来实现对由输送皮带17送过来的薄状面胚实现快切分隔成多条宽面条。The noodle cutting mechanism includes two cutting
面条切料机构上的两切面控制缸25通过外部控制其按需下降到设定的位置后,可以各个切面刀具29对进入到面条切料机构下方的输送皮带17上的面片进行压切,在压切的过程中薄状面胚被快切分隔成多条宽面条,从而继续向下游输送。After the two surface-cutting
当下部的各个切面刀具29使用一段时间且粘接在面块后,可以控制刀位调位单元旋转来将原来处于上部的各个切面刀具29进行调位,然后继续进行切面。When each
控制两个切面控制缸25向下伸出的幅度可以控制切面的深度和效果。The depth and the effect of the cut surface can be controlled by controlling the downward extension of the two cut
在上述任一方案中优选的是,在下部的各所述切面刀具29的底部安装有一压面防粘机构,所述压面防粘机构包括一防粘压面薄板30,所述防粘压面薄板30的两端向上翘起且呈水平吊挂部31,在所述防粘压面薄板30的底部沿其宽度方向依次间隔设置有若干个分别位于对应的切面刀具29底部的刮面长槽32,各所述刮面长槽32沿所述面条的输送方向设置且不会对上部和下部的切面刀具29的换位造成干涉,当个切面刀具29由对应的刮面长槽32穿过时可以将切面刀具29两侧粘连的面胚刮除。In any of the above schemes, preferably, a pressing surface anti-sticking mechanism is installed at the bottom of each of the
在切面的过程中为了保证切面的连贯性、防止面片粘连在刀具上,在此设置了压面防粘机构,在进行切面工作时由两个切面控制缸25控制活塞杆向下伸出带动切面辊轮27向下抵压对应的防粘压面薄板30,使得防粘压面薄板30的底部抵接在面片上,当面片被抵接后其仍然时可以被向下游输送的,此时控制刀位调位单元的刀具调位电机35旋转可以带动上部和下部的切片刀具实现旋转切面的状态,当然也可以直接保持刀具固定不动由输送皮带17继续向前输送面片来达到切面的目的,具体根据当前状态进行合理选择。In order to ensure the continuity of the cut surface and prevent the dough from sticking to the cutter during the cutting process, a surface-pressing anti-sticking mechanism is provided here, and the two cutting
防粘压面薄板30的底部喷涂防粘涂层,因此可以实现其底部防粘面的目的。The bottom of the anti-adhesive
另外,由于各个刮面长槽32配合对应的切面刀具29的设置,可以有效地实现在对应的切面刀具29旋转时就可以将切面刀具29上粘接的面块直接刮除,从而达到快速实现切面刀具29防粘的目的。In addition, due to the setting of each scraping surface
在上述任一方案中优选的是,所述防粘压面薄板30的两所述水平吊挂部31的顶部分别固定在一立柱33,两所述立柱33的顶部均活动伸至所述悬挂架2的上方,在各所述立柱33的外侧壁上分别套接有一吊挂弹簧34,两所述吊挂弹簧34的顶部分别固定在所述悬挂架2的底部,两所述吊挂弹簧34的底部均固定在对应位置处的所述水平吊挂部31的顶部。In any of the above schemes, it is preferred that the tops of the two
在此设置的吊挂弹簧34可以实现控制防粘压面薄板30在外部压力的作用下可以实现升降的目的,同时外力消失后还可以实现复位;同时设置的立柱33可以起到轴向定位的目的。The hanging
在上述任一方案中优选的是,所述刀位调位单元包括固定安装在对应位置处的所述切面控制缸25的活塞杆的一侧的刀具调位电机35,所述刀具调位电机35的电机轴与所述切面转动轴28的端部固连,所述刀具调位电机35通过旋转带动所述切面辊轮27的旋转,从而达到带动上部的各所述切面刀具29各下部的各所述切面刀具29旋转换位的目的。In any of the above schemes, it is preferred that the tool position adjustment unit includes a tool
刀位调位单元工作时主要是依靠刀具调位电机35的旋转可以带动整个切面转动轴28及其上的切面辊轮27的旋转,从而可以实现带动上部和下部的各切面刀具29旋转换位的目的,在旋转换位的同时实现利用各个刮面长槽32实现刮除刀具上的面块。When the knife position adjustment unit works, it mainly relies on the rotation of the knife
在所述导出弯管6的出料口处还设置有一面胚截断机构,所述面胚截断机构包括固定安装在所述悬挂架2底部的截断控制缸36,在所述截断控制缸36的活塞杆的底部固定安装有一截断电机37,所述截断电机37的电机轴处连接有一旋转截断刀盘38,所述旋转截断刀盘38的底部通过旋转将由导出弯管6的出料口处挤出的面胚实现按需截断。At the discharge port of the deriving elbow 6, a face blank cutting mechanism is also provided, and the dough cutting mechanism includes a cutting control cylinder 36 fixedly installed on the bottom of the
面胚截断机构可以根据设定需要的面条的长度进行周期性的控制截断控制缸36的升降,从而可以带动对应运转状态的截断控制缸36驱动旋转截断刀盘38边下移边旋转,从而将导出的面胚进行截断,保证面条的长度符合要求。The dough cutting mechanism can periodically control the lifting of the cutting control cylinder 36 according to the length of the noodles required for setting, so that the cutting control cylinder 36 of the corresponding operating state can be driven to rotate the
在所述导出弯管6的出料口处的下方还固定安装有一防护导料板39,所述防护导料板39位于所述旋转截断刀盘38下方且与其间隔设置。A protective
在截断面条的过程中利用防护导料板39可以起到防止截断刀盘直接接触输送皮带17的目的,更好地起到防护作用。Utilizing the protective
具体工作原理:Specific working principle:
本系统在进行工作时先将电源接通,启动整个系统的各零部件以及对应位置处配套设置的到位开关等传感器部件。When the system is working, first turn on the power supply, start the various parts of the whole system and the sensor components such as the in-position switch set at the corresponding position.
利用杂粮面团投料机构可以向内部投放粗粮杂粮面团,经过投放的面团会进入到面团成型输出机构,然后由动力传动机构可以控制面团成型输出机构对面胚成型速度的控制,成型的条状面胚会由面团成型输出机构向外输出,然后落入到输送皮带17送料机构,经过面胚辊压机构进行辊压成面片,然后在继续向前输送并经过面条切料机构的快切使其成为若干条的鲜宽面条,各宽鲜面条继续向前输送进入到面条烘干室3内部经过充分的烘干后输送至下游进行包装处理。Coarse grains and miscellaneous grains dough can be put into the interior by using the miscellaneous grains dough feeding mechanism, and the put dough will enter the dough forming output mechanism, and then the power transmission mechanism can control the dough forming output mechanism to control the dough forming speed, and the formed strip dough will be It is output by the dough forming output mechanism, and then falls into the feeding mechanism of the
面团成型输出机构工作时,由面团进料仓4送入到卧式螺旋成型机5内部的面团会在运动状态的螺旋输料轴7的作用下不断地向下游输送,最终面胚由右端出料口导出成条状面胚。在卧式螺旋成型机5的螺旋输料轴7工作的过程中可以通过控制动力传动机构的成型驱动电机的运转速度来调控向外导出面胚的速度,当成型驱动电机工作时会带动成型驱动带轮、成型从动带轮11运转并将动力输送至换向机构,经过换向机构的换向后送至螺旋输料轴7。皮带送料机构在运转时主要是依靠皮带输送机16的运转实现对输送皮带17的驱动,同时设置各个支撑托辊18的目的可以保证输送皮带17的良好支撑性,控制外部的驱动输送电机的输送速度可以控制整个输送皮带17及其上的面胚、面片、宽面条的输送速度。面胚辊压机构在此设置为可以由两个辊压调位缸21带动实现不同高度升降的结构,其可以实现根据不同的要求实现辊压处不同厚度的面片,从而控制后续的宽面条的厚度。在面胚压辊23辊压的过程中可快速的实现对由输送皮带17输送过来的面胚的高效辊压,保证辊压成型的效果。面条切料机构上的两切面控制缸25通过外部控制其按需下降到设定的位置后,可以各个切面刀具29对进入到面条切料机构下方的输送皮带17上的面片进行压切,在压切的过程中薄状面胚被快切分隔成多条宽面条,从而继续向下游输送。当下部的各个切面刀具29使用一段时间且粘接在面块后,可以控制刀位调位单元旋转来将原来处于上部的各个切面刀具29进行调位,然后继续进行切面。控制两个切面控制缸25向下伸出的幅度可以控制切面的深度和效果。在切面的过程中为了保证切面的连贯性、防止面片粘连在刀具上,在此设置了压面防粘机构,在进行切面工作时由两个切面控制缸25控制活塞杆向下伸出带动切面辊轮27向下抵压对应的防粘压面薄板30,使得防粘压面薄板30的底部抵接在面片上,当面片被抵接后其仍然时可以被向下游输送的,此时控制刀位调位单元的刀具调位电机35旋转可以带动上部和下部的切片刀具实现旋转切面的状态,当然也可以直接保持刀具固定不动由输送皮带17继续向前输送面片来达到切面的目的,具体根据当前状态进行合理选择。防粘压面薄板30的底部喷涂防粘涂层,因此可以实现其底部防粘面的目的。另外,由于各个刮面长槽32配合对应的切面刀具29的设置,可以有效地实现在对应的切面刀具29旋转时就可以将切面刀具29上粘接的面块直接刮除,从而达到快速实现切面刀具29防粘的目的。刀位调位单元工作时主要是依靠刀具调位电机35的旋转可以带动整个切面转动轴28及其上的切面辊轮27的旋转,从而可以实现带动上部和下部的各切面刀具29旋转换位的目的,在旋转换位的同时实现利用各个刮面长槽32实现刮除刀具上的面块。When the dough forming output mechanism is working, the dough fed into the horizontal screw forming machine 5 by the dough feeding bin 4 will be continuously conveyed downstream under the action of the moving screw feeding shaft 7, and finally the dough will come out from the right end. The feed port is exported into strip-shaped dough embryos. During the working process of the screw feeding shaft 7 of the horizontal screw forming machine 5, the speed of exporting the dough blank can be adjusted by controlling the running speed of the forming drive motor of the power transmission mechanism. When the forming drive motor is working, it will drive the forming drive. Belt pulley, forming driven pulley 11 run and power is delivered to the reversing mechanism, and sent to the screw feeding shaft 7 after the reversing of the reversing mechanism. The belt feeding mechanism mainly relies on the operation of the belt conveyor 16 to drive the
本系统能够对杂粮面团、面胚进行挤压成型,同时成型后可以实现对面胚的快速辊压成面,然后切割成鲜宽面条,最终由烘干室可以实现对宽面条的烘干成型,便于送入后续包装工序;本系统中在利用面团成型输出机构进行输送时能够有效地依靠动力传动机构上的换向机构实现对面胚的快速螺旋输送、挤压成型后导出,保证向外挤出条状面胚的速度;本系统中利用面胚辊压机构可以将输送状态下的条状面胚快速的辊压成薄片状的面片,等待后续的面条切料机构可以将其快速分切成若干条的宽面条,从而可以实现类似于人工制成的手擀宽面面条;在利用面条切料机构进行面条的分切的过程中本系统中还设计了压面防粘机构实现在切面的过程中防止面条被粘起,同时还能够有效地对已经站在各切面刀具29上的面块实现刮料脱料,从而保证切面工序的切面效果;系统中增设的面胚截断机构可以根据设定需要的面条的长度进行周期性的将导出的面胚进行截断,保证面条的长度符合要求,同时在截断面条的过程中利用防护导料板39可以起到防止截断刀盘直接接触输送皮带17的目的,更好地起到防护作用。This system can extrude miscellaneous grain dough and noodle embryos, and at the same time, after forming, it can quickly roll the opposite embryos into noodles, and then cut them into fresh wide noodles. Finally, the drying room can realize the drying and molding of wide noodles. It is convenient to send into the subsequent packaging process; when the dough forming output mechanism is used for conveying in this system, the reversing mechanism on the power transmission mechanism can be used to realize the rapid spiral conveying of the opposite dough, and the export after extrusion to ensure the outward extrusion The speed of the strip-shaped dough; in this system, the dough rolling mechanism can be used to quickly roll the strip-shaped dough in the conveying state into a thin sheet of dough, and wait for the subsequent noodle cutting mechanism to quickly cut it into several strips of lasagna, so as to realize hand-made lasagna similar to hand-made lasagna; in the process of cutting noodles by using the noodle cutting mechanism, this system also designed a surface-pressing and anti-sticking mechanism to realize the cutting surface In the process of preventing the noodles from sticking, it can also effectively scrape and remove the noodle blocks that have stood on the
以上各实施例仅用以说明本发明的技术方案,而非对其限制;尽管参照前述各实施例对本发明进行了详细的说明,本领域的普通技术人员应当理解:其依然可以对前述各实施例所记载的技术方案进行修改,或者对其中部分或者全部技术特征进行等同替换;而这些修改或者替换,并不使相应技术方案的本质脱离本发明各实施例技术方案的范围,其均应涵盖在本发明的权利要求和说明书的范围当中;对于本技术领域的技术人员来说,对本发明实施方式所做出的任何替代改进或变换均落在本发明的保护范围内。The above embodiments are only used to illustrate the technical solutions of the present invention, and are not intended to limit them; although the present invention has been described in detail with reference to the foregoing embodiments, those of ordinary skill in the art should understand that: it can still be applied to the foregoing embodiments Modifications to the technical solutions described in the examples, or equivalent replacement of some or all of the technical features; and these modifications or replacements do not make the essence of the corresponding technical solutions depart from the scope of the technical solutions of the embodiments of the present invention, and they shall cover Within the scope of the claims and description of the present invention; for those skilled in the art, any substitution, improvement or transformation made to the embodiments of the present invention falls within the protection scope of the present invention.
本发明未详述之处,均为本技术领域技术人员的公知技术。The parts of the present invention that are not described in detail are known technologies of those skilled in the art.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211403948.2A CN115606609B (en) | 2022-11-10 | 2022-11-10 | Special processing system of cereal full-dry noodless food |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211403948.2A CN115606609B (en) | 2022-11-10 | 2022-11-10 | Special processing system of cereal full-dry noodless food |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115606609A true CN115606609A (en) | 2023-01-17 |
| CN115606609B CN115606609B (en) | 2023-12-22 |
Family
ID=84878655
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202211403948.2A Active CN115606609B (en) | 2022-11-10 | 2022-11-10 | Special processing system of cereal full-dry noodless food |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115606609B (en) |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108656161A (en) * | 2018-04-18 | 2018-10-16 | 安徽佳谷豆食品有限公司 | A kind of automatic cutting transport device of rice cake |
| CN109717221A (en) * | 2018-12-24 | 2019-05-07 | 安徽青松食品有限公司 | A kind of production noodles noodle press and its application method |
| CN112617105A (en) * | 2020-12-22 | 2021-04-09 | 安徽燕之坊食品有限公司 | Processing technology of normal-temperature storage type grain-doped braised noodles |
| US20220039399A1 (en) * | 2018-09-11 | 2022-02-10 | König Maschinen Gesellschaft M.B.H. | Dough Strip Shaping Member Having A Cutting Device |
| CN216567950U (en) * | 2021-11-29 | 2022-05-24 | 南通昶昊机电制造有限公司 | Full-automatic stewed noodle production equipment |
| CN216968013U (en) * | 2021-12-24 | 2022-07-15 | 昆山科世茂包装材料有限公司 | Cutting assembly and low-temperature shrinkage cross-linked film production device using same |
| CN217065205U (en) * | 2022-01-12 | 2022-07-29 | 潍坊市农业科学院(山东省农业科学院潍坊市分院) | Multifunctional automatic noodle processing equipment |
-
2022
- 2022-11-10 CN CN202211403948.2A patent/CN115606609B/en active Active
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108656161A (en) * | 2018-04-18 | 2018-10-16 | 安徽佳谷豆食品有限公司 | A kind of automatic cutting transport device of rice cake |
| US20220039399A1 (en) * | 2018-09-11 | 2022-02-10 | König Maschinen Gesellschaft M.B.H. | Dough Strip Shaping Member Having A Cutting Device |
| CN109717221A (en) * | 2018-12-24 | 2019-05-07 | 安徽青松食品有限公司 | A kind of production noodles noodle press and its application method |
| CN112617105A (en) * | 2020-12-22 | 2021-04-09 | 安徽燕之坊食品有限公司 | Processing technology of normal-temperature storage type grain-doped braised noodles |
| CN216567950U (en) * | 2021-11-29 | 2022-05-24 | 南通昶昊机电制造有限公司 | Full-automatic stewed noodle production equipment |
| CN216968013U (en) * | 2021-12-24 | 2022-07-15 | 昆山科世茂包装材料有限公司 | Cutting assembly and low-temperature shrinkage cross-linked film production device using same |
| CN217065205U (en) * | 2022-01-12 | 2022-07-29 | 潍坊市农业科学院(山东省农业科学院潍坊市分院) | Multifunctional automatic noodle processing equipment |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115606609B (en) | 2023-12-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN207561280U (en) | A kind of steamed stuffed bun production line | |
| CN112088919A (en) | Full-automatic cake production line of steel band class | |
| CN216219824U (en) | A kind of noodle multi-stage rolling equipment | |
| CN115606609B (en) | Special processing system of cereal full-dry noodless food | |
| CN206851890U (en) | Full-automatic coarse cereals self heating flour stranding machine | |
| CN110463729A (en) | A kind of noodle extrusion process units | |
| CN210642192U (en) | A multifunctional pastry forming machine | |
| CN211211202U (en) | Mechanism is overlapped to multiunit section | |
| CN220422926U (en) | Feeding device of bread baking machine | |
| CN222284494U (en) | Shortening machine with adjusting function | |
| CN211129563U (en) | Fried instant noodle production device | |
| CN219182589U (en) | Noodle press | |
| CN212382014U (en) | Full-automatic cake production line of steel band class | |
| CN110558352A (en) | multifunctional pastry forming machine | |
| CN204560845U (en) | Instant noodle machine automatically | |
| CN111109317B (en) | Automatic dough pressing equipment for fried food | |
| CN216567969U (en) | Noodle shredding and cutting machine | |
| CN210538517U (en) | Noodle cutting equipment for processing fine dried noodles | |
| CN210809038U (en) | Pastry production line | |
| CN210445477U (en) | Dough cutting mechanism | |
| CN218195609U (en) | Saqima production slitting forming device | |
| CN108497007B (en) | Automatic blanking dough pressing shaper | |
| CN223274784U (en) | Instant braised noodle cake forming equipment | |
| CN220587370U (en) | Automatic circulation dough pressing machine | |
| CN223000640U (en) | Intelligent food cutting equipment |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| TR01 | Transfer of patent right |
Effective date of registration: 20241118 Address after: Economic Park, Caitang Town, Shan County, Heze City, Shandong Province, 274300 Patentee after: Shandong Jibing Food Co.,Ltd. Country or region after: China Address before: Economic Park, Caitang Town, Shan County, Heze City, Shandong Province, 274300 Patentee before: Shanxian Luyixin Flour Co.,Ltd. Country or region before: China |
|
| TR01 | Transfer of patent right |