CN115582481A - Continuous stamping and forming device for circular saw blade - Google Patents
Continuous stamping and forming device for circular saw blade Download PDFInfo
- Publication number
- CN115582481A CN115582481A CN202211353774.3A CN202211353774A CN115582481A CN 115582481 A CN115582481 A CN 115582481A CN 202211353774 A CN202211353774 A CN 202211353774A CN 115582481 A CN115582481 A CN 115582481A
- Authority
- CN
- China
- Prior art keywords
- die
- connecting rod
- saw blade
- circular saw
- groove
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000000463 material Substances 0.000 claims abstract description 33
- 230000005540 biological transmission Effects 0.000 claims description 10
- 238000004891 communication Methods 0.000 claims description 2
- 238000000465 moulding Methods 0.000 claims 2
- 238000003756 stirring Methods 0.000 claims 1
- 230000000717 retained effect Effects 0.000 abstract 1
- 238000004080 punching Methods 0.000 description 11
- 238000005452 bending Methods 0.000 description 8
- 238000010586 diagram Methods 0.000 description 6
- 239000002184 metal Substances 0.000 description 4
- 238000000034 method Methods 0.000 description 4
- 230000009471 action Effects 0.000 description 3
- 230000008569 process Effects 0.000 description 2
- 239000002994 raw material Substances 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 230000013011 mating Effects 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 238000012805 post-processing Methods 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 238000003672 processing method Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D28/00—Shaping by press-cutting; Perforating
- B21D28/02—Punching blanks or articles with or without obtaining scrap; Notching
- B21D28/14—Dies
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D28/00—Shaping by press-cutting; Perforating
- B21D28/02—Punching blanks or articles with or without obtaining scrap; Notching
- B21D28/04—Centering the work; Positioning the tools
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D45/00—Ejecting or stripping-off devices arranged in machines or tools dealt with in this subclass
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
Abstract
Description
技术领域technical field
本发明涉及连续冲压模具领域,特别涉及一种圆锯片连续冲压成型装置。The invention relates to the field of continuous stamping dies, in particular to a continuous stamping forming device for circular saw blades.
背景技术Background technique
连续冲压是一种金属加工方法,可能包括冲压、拉深、折弯和其他金属原材料的方法,并结合自动送料系统,进料系统推动金属料带通过连续模具的所有工位,连续冲模是指用一条原材料在一个冲模上的不同工位同时完成多个冲压工序的冷冲压模具,该条料移动一个固定的距离,每冲程一次,直到成品,在加工圆锯片时会采用了连续冲压模具对板料进行冲裁,可以将圆锯片的中心孔和外圆进行依次冲裁,从而可以获得圆锯片的外形,之后对其进行热处理等工具即可;Continuous stamping is a metal processing method that may include stamping, deep drawing, bending and other methods of metal raw materials, combined with an automatic feeding system, the feeding system pushes the metal strip through all stations of the continuous die, continuous die refers to A cold stamping die that uses a strip of raw material to complete multiple stamping processes at different positions on a die at the same time. The strip moves a fixed distance, one stroke per stroke, until the finished product. Continuous stamping dies are used when processing circular saw blades For punching the sheet, the center hole and the outer circle of the circular saw blade can be punched sequentially, so that the shape of the circular saw blade can be obtained, and then heat treatment and other tools can be used for it;
但现有的圆锯片连续冲压模具存在一定的弊端,在对圆锯片完成冲裁后,由于圆锯片的边缘处会有一圈锯齿,如果直接将锯齿落下容易受到落料槽的影响,使得锯齿会与设备相撞击,尤其是在锯齿竖直掉落时,容易使得锯齿发生弯曲或者变形,不仅影响圆锯片的尺寸和精度,还影响后期加工处理,还有在落料时由于凹模和凸模之间相配合时,由于板料的边缘容易存在毛边或者毛刺,此时板料容易被卡在落料槽处,使得落料槽中的板料在下一次冲裁时被其它的板料推出才能落料。However, there are certain disadvantages in the existing continuous stamping dies for circular saw blades. After punching the circular saw blades, there will be a circle of saw teeth on the edge of the circular saw blades. If the saw teeth are dropped directly, it is easy to be affected by the blanking groove The saw teeth will collide with the equipment, especially when the saw teeth fall vertically, it is easy to cause the saw teeth to bend or deform, which not only affects the size and accuracy of the circular saw blade, but also affects the post-processing. When the die and the punch are matched, because there are burrs or burrs on the edge of the sheet, the sheet is easy to be stuck at the blanking chute, so that the sheet in the blanking chute will be punched by other punches during the next punching. The sheet can only be blanked when it is pushed out.
发明内容Contents of the invention
本发明的主要目的在于提供一种圆锯片连续冲压成型装置,可以有效解决背景技术中的技术问题。The main purpose of the present invention is to provide a circular saw blade continuous stamping forming device, which can effectively solve the technical problems in the background art.
为实现上述目的,本发明采取的技术方案为:In order to achieve the above object, the technical scheme that the present invention takes is:
一种圆锯片连续冲压成型装置,包括由上而下依次安装的上模座、凸模、上模固定板、凹模、下模座,所述凹模和下模座的中间开设有落料槽,所述凹模的顶端两侧设置有导料板,所述上模固定板、凹模和下模座之间且靠近导料板处安装有升降结构,所述升降结构位于落料槽的一侧;A continuous stamping and forming device for circular saw blades, comprising an upper mold base, a punch, an upper mold fixing plate, a die, and a lower mold base installed sequentially from top to bottom. Material trough, the two sides of the top of the die are provided with material guide plates, and a lifting structure is installed between the fixed plate of the upper die, the die and the lower die base and close to the material guide plate, and the lifting structure is located at the blanking one side of the groove;
所述升降结构包括预留槽和连杆,所述预留槽开设于凹模的内部,且预留槽位于落料槽的一侧,所述连杆位于预留槽的内部,所述连杆的顶端设置有限位块,且上模固定板的下表面且位于与限位块相对应处焊接有配合块,所述下模座的顶端且位于连杆的底端开设有固定槽,所述固定槽的内部设置有第一弹簧,且第一弹簧与连杆的底端相接触。The lifting structure includes a reserved groove and a connecting rod, the reserved groove is opened inside the die, and the reserved groove is located on one side of the blanking groove, the connecting rod is located inside the reserved groove, and the connecting rod is located inside the reserved groove. The top of the bar is provided with a limit block, and the lower surface of the upper die fixing plate is welded with a fitting block corresponding to the limit block, and the top of the lower die base is provided with a fixing groove at the bottom end of the connecting rod. A first spring is arranged inside the fixing groove, and the first spring is in contact with the bottom end of the connecting rod.
作为本发明优选的一种技术方案,所述预留槽的顶端开设有配合槽,且配合槽的形状与限位块和配合块均相匹配,且配合槽的深度大于限位块的厚度。As a preferred technical solution of the present invention, a matching groove is opened at the top of the reserved groove, and the shape of the matching groove matches both the limit block and the matching block, and the depth of the matching groove is greater than the thickness of the limit block.
作为本发明优选的一种技术方案,所述凹模的内部且位于落料槽和预留槽之间设置有拨料结构,所述拨料结构包括放置腔,所述放置腔开设于落料槽和预留槽之间,且落料槽、放置腔与预留槽相连通,所述放置腔的内部设置有转动销、连接杆和弯杆,所述转动销架设在放置腔的内部,且转动销与连接杆转动连接,且连接杆和弯杆为一体,所述连杆的中间设置有拨杆,且拨杆的一端与弯杆相连接,且拨杆的另一端内部套设有第二弹簧。As a preferred technical solution of the present invention, a material shifting structure is provided inside the die and between the blanking trough and the reserved groove, the material shifting structure includes a placement cavity, and the placement cavity is opened in the blanking Between the groove and the reserved groove, and the blanking groove, the placement cavity is connected with the reserved groove, the inside of the placement cavity is provided with a rotating pin, a connecting rod and a bending rod, and the rotating pin is set inside the placement cavity, And the rotating pin is connected to the connecting rod in rotation, and the connecting rod and the bending rod are integrated, a driving rod is arranged in the middle of the connecting rod, and one end of the driving rod is connected with the bending rod, and the other end of the driving rod is sleeved with a Second spring.
作为本发明优选的一种技术方案,所述第二弹簧的一端位于拨杆的内部,且第二弹簧的另一端与预留槽相接触,所述放置腔与预留槽相通处开设有倒斜角。As a preferred technical solution of the present invention, one end of the second spring is located inside the lever, and the other end of the second spring is in contact with the reserved groove, and an inverted opening is opened at the communication place between the placement cavity and the reserved groove. bevel.
作为本发明优选的一种技术方案,所述凹模的内部且位于落料槽的下端设置有支撑结构,所述支撑结构包括固定盘,所述固定盘通过螺纹设置于落料槽的下端,所述固定盘的表面设置有限位环,所述固定盘和三个限位环之间安装有转动环,且转动环与固定盘转动连接,所述固定盘的表面设置有若干个支撑杆,且转动环和每个支撑杆之间均连接有第三弹簧。As a preferred technical solution of the present invention, a support structure is provided inside the die and at the lower end of the blanking chute, the support structure includes a fixed plate, and the fixed plate is threadedly arranged at the lower end of the blanking chute, A limiting ring is arranged on the surface of the fixed disk, a rotating ring is installed between the fixed disk and the three limiting rings, and the rotating ring is rotatably connected to the fixed disk, and several support rods are arranged on the surface of the fixed disk, And a third spring is connected between the rotating ring and each supporting rod.
作为本发明优选的一种技术方案,所述支撑杆的一端设置有销轴,且支撑杆与销轴转动连接,所述固定盘的表面位于支撑杆的中间焊接有限位销轴,且支撑杆的另一端与第三弹簧相连接。As a preferred technical solution of the present invention, one end of the support rod is provided with a pin shaft, and the support rod is rotatably connected to the pin shaft, the surface of the fixed plate is located in the middle of the support rod and is welded with a limit pin shaft, and the support rod The other end is connected with the third spring.
作为本发明优选的一种技术方案,所述升降结构的下端和支撑结构之间设置有控制结构,所述控制结构包括套筒,所述套筒设置于连杆的下端,且连杆的下端设置有传动螺纹,所述连杆的下端通过传动螺纹与套筒连接,所述预留槽的底端螺纹连接有挡环,且挡环位于套筒的下方,所述固定盘的边缘焊接有导向环,所述转动环的侧壁焊接有固定扣,所述套筒的外圆柱面缠绕有连接绳,且连接绳贯穿导向环的内部并与固定扣相连接。As a preferred technical solution of the present invention, a control structure is provided between the lower end of the lifting structure and the support structure, the control structure includes a sleeve, the sleeve is arranged at the lower end of the connecting rod, and the lower end of the connecting rod A transmission thread is provided, the lower end of the connecting rod is connected with the sleeve through the transmission thread, the bottom end of the reserved groove is threaded with a retaining ring, and the retaining ring is located below the sleeve, and the edge of the fixed plate is welded with In the guide ring, the side wall of the rotating ring is welded with a fixing buckle, and the outer cylindrical surface of the sleeve is wound with a connecting rope, and the connecting rope runs through the inside of the guiding ring and is connected with the fixing buckle.
作为本发明优选的一种技术方案,所述连接绳的端部与转动环相系合,且连接绳与转动环边缘相切。As a preferred technical solution of the present invention, the end of the connecting rope is tied to the rotating ring, and the connecting rope is tangent to the edge of the rotating ring.
作为本发明优选的一种技术方案,所述上模座和上模固定板的四角设置有导柱和导套,且凸模的四个拐角与导柱滑动连接,所述凸模的中间设置有模柄,且模柄贯穿上模座的内部,所述凸模的底端中间与凹模的落料槽相对齐,所述凹模与下模座通过螺栓相固定。As a preferred technical solution of the present invention, the four corners of the upper die base and the upper die fixing plate are provided with guide posts and guide sleeves, and the four corners of the punch are slidably connected with the guide posts, and the middle of the punch is set There is a die handle, and the die handle runs through the inside of the upper die base, the middle of the bottom end of the punch is aligned with the blanking groove of the die, and the die and the lower die base are fixed by bolts.
本发明的有益效果如下:The beneficial effects of the present invention are as follows:
设置有升降结构,通过第一弹簧推动连杆升降从而使得限位块可以浮动,从而在推动制作圆锯片板料时可以对齐进行限位,且通过升降的限位块使得只有板料的切口与配合块和限位块相匹配才能进行限位,避免常规的限位装置横向浮动与不是限位的切口相扣合的情况;It is equipped with a lifting structure, and the first spring pushes the connecting rod up and down so that the limit block can float, so that it can be aligned and limited when pushing to make the circular saw blade, and only the incision of the plate can be made by the lifting limit block The limit can only be carried out by matching with the matching block and the limit block, avoiding the situation where the conventional limit device moves horizontally and buckles the notch that is not a limit;
设置有拨料结构,在合模时连杆被下压降下来,此时连接杆可以绕着转动销进行转动,朝着一个方向转动时可以将刚刚冲裁出的锯片进行拨动,从而使得锯片可以从落料槽内部落下,避免锯片滞留在落料槽的内部;在连杆升起来时,连接杆进行反向转动使得连接杆收纳到放置腔中,在冲裁时不会影响模具正常冲裁;There is a material dialing structure, the connecting rod is pressed down when the mold is closed, at this time the connecting rod can rotate around the rotating pin, and when turning in one direction, the saw blade just punched out can be moved, so that The saw blade can fall from the inside of the blanking trough, and the saw blade is prevented from staying in the blanking trough; when the connecting rod is raised, the connecting rod rotates in the opposite direction so that the connecting rod is stored in the placement cavity, and there is no need for punching. It will affect the normal punching of the mold;
通过设置拨杆,将拨杆进行拨动时保证连杆升降时均能弯杆相接触,保证拨料结构正常工作,且拨杆在预留槽中移动,可以对连杆升降起到限位作用;By setting the lever, when the lever is toggled, it is ensured that the connecting rod can be in contact with the bent rod when it is raised and lowered, so that the material shifting structure can work normally, and the lever moves in the reserved groove, which can limit the lifting and lowering of the connecting rod. ;
设置有支撑结构,在常态下支撑杆从落料槽中露出,在被拨料结构拨动的圆锯片水平落到支撑杆之间,圆锯片后期落下比较平稳,避免圆锯片倾斜落下造成圆锯片边缘的锯齿与设备相接触,不会造成圆锯片的锯齿发生形变和发生弯曲;There is a support structure, under normal conditions, the support rods are exposed from the blanking trough, and the circular saw blades moved by the dial structure fall horizontally between the support rods, and the circular saw blades fall relatively smoothly in the later stage, avoiding the circular saw blades from falling obliquely Cause the saw teeth on the edge of the circular saw blade to be in contact with the equipment, and will not cause deformation and bending of the saw teeth of the circular saw blade;
设置有控制结构,在连杆下降时连接绳拉动转动环进行转动,从而可以将支撑杆收纳起来,从而可以将圆锯片平稳落下;连杆升起时连接绳处于松弛状态,从而支撑杆可以展出对圆锯片进行支撑;There is a control structure, when the connecting rod is lowered, the connecting rope pulls the rotating ring to rotate, so that the support rod can be stored, so that the circular saw blade can be dropped smoothly; when the connecting rod is raised, the connecting rope is in a loose state, so that the supporting rod can be Exhibited support for circular saw blades;
通过升降结构带动拨料结构、支撑结构和控制结构进行统一的运转,并使得拨料结构、支撑结构和控制结构相互协作,将冲裁好的圆锯片进行拨动后平稳落下,避免圆锯片无法正常落料或者落料后锯齿发生弯曲的情况。The lifting structure drives the material shifting structure, support structure and control structure to operate in a unified manner, and makes the material shifting structure, support structure and control structure cooperate with each other, and the punched circular saw blade is moved and falls smoothly to avoid circular saw blades. The sheet cannot be blanked normally or the saw teeth are bent after blanking.
附图说明Description of drawings
图1为本发明一种圆锯片连续冲压成型装置的整体结构示意图;Fig. 1 is a schematic diagram of the overall structure of a circular saw blade continuous stamping forming device of the present invention;
图2为本发明一种圆锯片连续冲压成型装置的结构拆分示意图;Fig. 2 is a structural disassembly schematic diagram of a circular saw blade continuous stamping forming device of the present invention;
图3为本发明一种圆锯片连续冲压成型装置的内部结构示意图;Fig. 3 is a schematic diagram of the internal structure of a circular saw blade continuous stamping forming device of the present invention;
图4为图3中A处放大图;Figure 4 is an enlarged view of A in Figure 3;
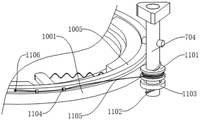
图5为图4中B处放大图;Figure 5 is an enlarged view at B in Figure 4;
图6为本发明一种圆锯片连续冲压成型装置的支撑结构示意图;Fig. 6 is a schematic diagram of a supporting structure of a circular saw blade continuous stamping forming device of the present invention;
图7为本发明一种圆锯片连续冲压成型装置的支撑结构拆分示意图;Fig. 7 is a disassembled schematic diagram of a supporting structure of a circular saw blade continuous stamping forming device according to the present invention;
图8为本发明一种圆锯片连续冲压成型装置的控制结构示意图。Fig. 8 is a schematic diagram of the control structure of a circular saw blade continuous stamping forming device according to the present invention.
图中:1、上模座;2、凸模;3、上模固定板;4、凹模;5、下模座;6、导料板;7、升降结构;8、落料槽;9、拨料结构;10、支撑结构;11、控制结构;701、配合块;702、预留槽;703、第一弹簧;704、连杆;705、限位块;706、固定槽;901、放置腔;902、转动销;903、连接杆;904、弯杆;905、拨杆;906、第二弹簧;1001、固定盘;1002、限位环;1003、支撑杆;1004、第三弹簧;1005、转动环;1101、套筒;1102、传动螺纹;1103、挡环;1104、导向环;1105、连接绳;1106、固定扣。In the figure: 1. Upper mold base; 2. Punch mold; 3. Upper mold fixing plate; 4. Die; 5. Lower mold base; 6. Material guide plate; 7. Lifting structure; 8. Blanking trough; 9 1. Dial structure; 10. Support structure; 11. Control structure; 701. Cooperating block; 702. Reserved slot; 703. First spring; 704. Connecting rod; 705. Limiting block; Placement cavity; 902, rotating pin; 903, connecting rod; 904, bent rod; 905, driving rod; 906, second spring; 1001, fixed plate; 1002, limit ring; 1003, support rod; 1005, rotating ring; 1101, sleeve; 1102, transmission thread; 1103, retaining ring; 1104, guide ring; 1105, connecting rope; 1106, fixed buckle.
具体实施方式detailed description
为使本发明实现的技术手段、创作特征、达成目的与功效易于明白了解,下面结合具体实施方式,进一步阐述本发明。In order to make the technical means, creative features, goals and effects achieved by the present invention easy to understand, the present invention will be further described below in conjunction with specific embodiments.
如图1-8所示,一种圆锯片连续冲压成型装置,包括由上而下依次安装的上模座1、凸模2、上模固定板3、凹模4、下模座5,上模座1和上模固定板3的四角设置有导柱和导套,且凸模2的四个拐角与导柱滑动连接,凸模2的中间设置有模柄,且模柄贯穿上模座1的内部,凸模2的底端中间与凹模4的落料槽8相对齐,凹模4与下模座5通过螺栓相固定,将上模座1、凸模2、上模固定板3、凹模4、下模座5进行组装,凸模2的模柄与压力机相连接,从而压力机在升降时可以使得模具可以进行合模和开模,进而使得凸模2的下表面凸出部位与凹模4进行闭合或者开启,且期间凸模2沿着导柱导套进行升降,保证凸模2与凹模4精确对齐,凹模4和下模座5的中间开设有落料槽8,由于开设有两个大小不同的落料槽8,在冲裁时,小的落料槽8冲裁处圆锯片转轴部分,大的落料槽8将冲裁出圆锯片的锯齿的形状或者外圆片形状,凹模4的顶端两侧设置有导料板6,工作时在牵引机的拉动下将板料沿着导料板6进行输送,避免板料发生偏移,上模固定板3、凹模4和下模座5之间且靠近导料板6处安装有升降结构7,升降结构7位于落料槽8的一侧,通过升降结构7带动拨料结构9、支撑结构10和控制结构11进行统一的运转,并使得拨料结构9、支撑结构10和控制结构11相互协作,将冲裁好的圆锯片进行拨动后平稳落下,避免圆锯片无法正常落料或者落料后锯齿发生弯曲的情况;As shown in Figure 1-8, a circular saw blade continuous stamping and forming device includes an
升降结构7包括预留槽702和连杆704,预留槽702开设于凹模4的内部,且预留槽702位于落料槽8的一侧,连杆704位于预留槽702的内部,连杆704沿着预留槽702的内部进行升降,连杆704的顶端设置有限位块705,且上模固定板3的下表面且位于与限位块705相对应处焊接有配合块701,由于配合块701和限位块705的截面形状相同且位置对应,此时在上模固定板3随着凸模2进行升降时,上模固定板3的配合块701与限位块705相接触,然后配合块701将限位块705推动到预留槽702的内部,不影响配合块701和限位块705对板料的进行限位,下模座5的顶端且位于连杆704的底端开设有固定槽706,固定槽706的内部设置有第一弹簧703,且第一弹簧703与连杆704的底端相接触,连杆704下降时第一弹簧703被压缩在固定槽706中,开模时,凸模2和上模固定板3随着一起升起,此时在固定槽706中的第一弹簧703弹力作用下使得连杆704沿着预留槽702的内部进行升起,使得连杆704的限位块705被抬起,从而可以通过浮起的限位块705对板料的限位槽口进行限位。The lifting
本实施例中,预留槽702的顶端开设有配合槽,且配合槽的形状与限位块705和配合块701均相匹配,且配合槽的深度大于限位块705的厚度,在配合块701和限位块705配合时,可以通过配合块701将限位块705进行推动,将带有槽口的板料卡紧在配合块701和限位块705处,避免冲裁时发生相对位置,提高冲裁板料的精度,通过升降结构7的第一弹簧703推动连杆704升降从而使得限位块705可以浮动,从而在推动制作圆锯片板料时可以对齐进行限位,且通过升降的限位块705使得只有板料的切口与配合块701和限位块705相匹配才能进行限位,避免常规的限位装置横向浮动与不是限位的切口相扣合的情况。In this embodiment, the top of the
本实施例中,凹模4的内部且位于落料槽8和预留槽702之间设置有拨料结构9,拨料结构9包括放置腔901,放置腔901开设于落料槽8和预留槽702之间,且落料槽8、放置腔901与预留槽702相连通,在落料槽8、放置腔901和预留槽702相连通时,保证连接杆903和弯杆904有足够的转动空间,放置腔901的内部设置有转动销902、连接杆903和弯杆904,转动销902架设在放置腔901的内部,且转动销902与连接杆903转动连接,靠近落料槽8处的连接杆903一端转动到最高处位置,此时连接杆903仍然位于放置腔901的内部,在连接杆903转动到水平位置时,连接杆903从放置腔901中将连接杆903的端部露出,连接杆903和弯杆904为一体,连杆704的中间设置有拨杆905,且拨杆905的一端与弯杆904相连接,且拨杆905的另一端内部套设有第二弹簧906,拨杆905在升降时会与弯杆904相接触,从而带动弯杆904进行偏转,且通过第二弹簧906推动拨杆905与弯杆904相接触,通过设置拨杆905,将拨杆905进行拨动时保证连杆704升降时均能弯杆904相接触,保证拨料结构9正常工作,且拨杆905在预留槽702中移动,可以对连杆704升降起到限位作用。In this embodiment, a
本实施例中,第二弹簧906的一端位于拨杆905的内部,且第二弹簧906的另一端与预留槽702相接触,放置腔901与预留槽702相通处开设有倒斜角,通过斜角可以在拨杆905移动到限位的地方时使得拨杆905中的第二弹簧906被压缩,从而使得拨杆905与弯杆904的端部始终接触,避免拨杆905与弯杆904发生松动,在合模时连杆704被下压降下来,此时连接杆903可以绕着转动销902进行转动,朝着一个方向转动时可以将刚刚冲裁出的锯片进行拨动,从而使得锯片可以从落料槽8内部落下,避免锯片滞留在落料槽8的内部;在连杆704升起来时,连接杆903进行反向转动使得连接杆903收纳到放置腔901中,在冲裁时不会影响模具正常冲裁。In this embodiment, one end of the
本实施例中,凹模4的内部且位于落料槽8的下端设置有支撑结构10,支撑结构10包括固定盘1001,固定盘1001通过螺纹设置于落料槽8的下端,通过将固定盘1001旋在落料槽8的下端,并保证固定盘1001的内径大于落料槽8的内径,保证落料可以从固定盘1001中落下,固定盘1001的表面设置有限位环1002,固定盘1001和限位环1002之间安装有转动环1005,且转动环1005与固定盘1001转动连接,固定盘1001、限位环1002、转动环1005之间的轴线均相同,固定盘1001的表面设置有若干个支撑杆1003,保证转动环1005转动时支撑杆1003随之摆动时不会对其产生影响,且转动环1005和每个支撑杆1003之间均连接有第三弹簧1004,在转动环1005转动时会将第三弹簧1004拉紧,此时转动环1005会沿着第三弹簧1004的方向将固定盘1001进行拉动,在常态下支撑杆1003从落料槽8中露出,在被拨料结构9拨动的圆锯片水平落到支撑杆1003之间,圆锯片后期落下比较平稳,避免圆锯片倾斜落下造成圆锯片边缘的锯齿与设备相接触,不会造成圆锯片的锯齿发生形变和发生弯曲。In this embodiment, the inside of the
本实施例中,支撑杆1003的一端设置有销轴,且支撑杆1003与销轴转动连接,固定盘1001的表面位于支撑杆1003的中间焊接有限位销轴,且支撑杆1003的另一端与第三弹簧1004相连接,在第三弹簧1004被拉动状态时此时支撑杆1003发生偏转,使得落下的料板可以再次从支撑杆1003中落下,第三弹簧1004处于松弛状态时会抵着支撑杆1003与限位销轴进行接触,可以对落下的圆锯片进行支撑。In this embodiment, one end of the
本实施例中,升降结构7的下端和支撑结构10之间设置有控制结构11,控制结构11包括套筒1101,套筒1101设置于连杆704的下端,且连杆704的下端设置有传动螺纹1102,该传动螺纹1102类似于儿童玩具的手推飞盘结构相近,只要手推飞盘与螺纹杆相互运动飞盘即可转动,连杆704的下端通过传动螺纹1102与套筒1101连接,此时转动的套筒1101可以相对于连杆704进行转动一定圈数,预留槽702的底端螺纹连接有挡环1103,且挡环1103位于套筒1101的下方,通过挡环1103避免套筒1101发生上下浮动,保证套筒1101与连杆704之间转动,固定盘1001的边缘焊接有导向环1104,转动环1005的侧壁焊接有固定扣1106,套筒1101的外圆柱面缠绕有连接绳1105,且连接绳1105贯穿导向环1104的内部并与固定扣1106相连接,通过套筒1101转动可以将连接绳1105进行收紧,从而连接绳1105的端部可以带动转动环1005转动,从而使得转动环1005与固定盘1001发生相对移动,在套筒1101与连接绳1105之间发生松弛状态时,此时在转动环1005与固定盘1001之间的第三弹簧1004的作用下使得固定盘1001和转动环1005恢复原状态。In this embodiment, a
本实施例中,连接绳1105的端部与转动环1005相系合,且连接绳1105与转动环1005边缘相切转动环1005转动一定角度,可以通过导向环1104防止连接绳1105与固定盘1001和转动环1005卡紧或者打结,在连杆704下降时连接绳1105拉动转动环1005进行转动,从而可以将支撑杆1003收纳起来,从而可以将圆锯片平稳落下;连杆704升起时连接绳1105处于松弛状态,从而支撑杆1003可以展出对圆锯片进行支撑。In this embodiment, the end of the connecting
需要说明的是,本发明为一种圆锯片连续冲压成型装置,在使用前,准备好制作圆锯片的板料,然后将板料贯穿上模固定板3与凹模4之间,并将板料的一端通过牵引机构将其进行牵引,使得板料可以连续不断的进入到模具的内部,然后在合模时,通过压力机将凸模2和上模固定板3进行下降,此时会通过上模固定板3下表面的预定块将板料边缘冲出限位槽口,且通过凸模2下表面冲出一个与切割机的转轴相对应的孔,开模时,刚刚被冲出小孔移动到较大的落料槽8处,此时可以升降的限位块705在与限位槽口相扣合,从而可以使得板料前进一定长度,在再次合模时,凸模2和上模固定板3一起向下移动,配合块701将限位块705压紧,然后此时升降结构7的拨杆905带动弯杆904进行摆动,使得连接杆903收起来,与此同时,连杆704的传动螺纹1102与套筒1101相配合,从而使得连接绳1105拉动转动环1005在固定盘1001中转动,从而转动环1005的第三弹簧1004拉动支撑杆1003进行摆动,此时之前落下的板料会从支撑杆1003落下,板料不会倾斜落下,在开模时,连杆704的传动螺纹1102与套筒1101反向转动,从而连接绳1105处于松弛状态,此时在第三弹簧1004的作用下使得转动环1005和支撑杆1003相互靠近,使得支撑杆1003支撑在落料槽8中,与此同时,连杆704升起的同时会使得拨杆905将弯杆904和连接杆903进行转动,从而将刚刚冲裁的板料进行拨动,避免板料卡紧在落料槽8处,保证板料顺利从落料槽8中落下,然后继续升起凸模2和上模固定板3时,配合块701与限位块705分离,由于限位块705的边缘处开有倒角,从而在配合块701和限位块705刚刚分离时方便将板料继续被牵引机拉动,在遇到下一个限位槽口时在第一弹簧703的作用下将限位块705插入到限位槽口处,此时可以进行下一次冲压,往复如此可以通过该模具可以实现圆锯片的冲孔和落料的工序。It should be noted that the present invention is a continuous stamping and forming device for circular saw blades. Before use, the sheet material for making circular saw blades is prepared, and then the sheet material is passed through between the upper
以上显示和描述了本发明的基本原理和主要特征和本发明的优点。本行业的技术人员应该了解,本发明不受上述实施例的限制,上述实施例和说明书中描述的只是说明本发明的原理,在不脱离本发明精神和范围的前提下,本发明还会有各种变化和改进,这些变化和改进都落入要求保护的本发明范围内。本发明要求保护范围由所附的权利要求书及其等效物界定。The basic principles and main features of the present invention and the advantages of the present invention have been shown and described above. Those skilled in the industry should understand that the present invention is not limited by the above-mentioned embodiments. What are described in the above-mentioned embodiments and the description only illustrate the principle of the present invention. Without departing from the spirit and scope of the present invention, the present invention will also have Variations and improvements are possible, which fall within the scope of the claimed invention. The protection scope of the present invention is defined by the appended claims and their equivalents.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211353774.3A CN115582481B (en) | 2022-11-01 | 2022-11-01 | A circular saw blade continuous stamping forming device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211353774.3A CN115582481B (en) | 2022-11-01 | 2022-11-01 | A circular saw blade continuous stamping forming device |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115582481A true CN115582481A (en) | 2023-01-10 |
| CN115582481B CN115582481B (en) | 2024-12-13 |
Family
ID=84782083
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202211353774.3A Active CN115582481B (en) | 2022-11-01 | 2022-11-01 | A circular saw blade continuous stamping forming device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115582481B (en) |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP3016673U (en) * | 1995-04-06 | 1995-10-09 | 日本ダイスチール株式会社 | Device for removing punching scraps in a paper machine punching device |
| CN211707851U (en) * | 2019-12-14 | 2020-10-20 | 长安大学 | Thin type machining device for parts with holes |
| KR102180542B1 (en) * | 2019-11-13 | 2020-11-19 | 킨더스 주식회사 | Punching machine |
| CN212703929U (en) * | 2020-06-17 | 2021-03-16 | 日照海泰克工具设备有限公司 | Frock for numerical control punch for circular saw blade base member processing |
| CN112823950A (en) * | 2019-11-20 | 2021-05-21 | 湖南工业大学 | Be used for energy storage flywheel to prevent blockking up perforating device |
| CN115121695A (en) * | 2022-07-07 | 2022-09-30 | 深圳市冠宏达科技有限公司 | Die-cut device of reinforcement piece that high accuracy is strikeed for a short time |
-
2022
- 2022-11-01 CN CN202211353774.3A patent/CN115582481B/en active Active
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP3016673U (en) * | 1995-04-06 | 1995-10-09 | 日本ダイスチール株式会社 | Device for removing punching scraps in a paper machine punching device |
| KR102180542B1 (en) * | 2019-11-13 | 2020-11-19 | 킨더스 주식회사 | Punching machine |
| CN112823950A (en) * | 2019-11-20 | 2021-05-21 | 湖南工业大学 | Be used for energy storage flywheel to prevent blockking up perforating device |
| CN211707851U (en) * | 2019-12-14 | 2020-10-20 | 长安大学 | Thin type machining device for parts with holes |
| CN212703929U (en) * | 2020-06-17 | 2021-03-16 | 日照海泰克工具设备有限公司 | Frock for numerical control punch for circular saw blade base member processing |
| CN115121695A (en) * | 2022-07-07 | 2022-09-30 | 深圳市冠宏达科技有限公司 | Die-cut device of reinforcement piece that high accuracy is strikeed for a short time |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115582481B (en) | 2024-12-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN205949709U (en) | Horizontal hunting formula dynamic sending machine in mould | |
| CN116727543B (en) | Stamping forming die for sheet metal plate furniture | |
| CN111872232A (en) | A kind of metal processing piece roll forming device and forming method | |
| CN112828144B (en) | A continuous stamping die for rounding the jacks of tiny and precise communication components | |
| CN215143927U (en) | Stamping die for top rod hook of security door | |
| CN207857685U (en) | Metal material belt punching mechanism | |
| CN115582481B (en) | A circular saw blade continuous stamping forming device | |
| CN207709657U (en) | Hard alloy sawtooth sheetmolding mold | |
| CN217192206U (en) | Drawing die material returning mechanism | |
| CN211564203U (en) | A kind of hydraulic composite mold for edge-inward inclined bending fasteners | |
| CN206169024U (en) | A system of processing for processing sliding support kerve | |
| CN211746549U (en) | Meat pie stamping forming equipment | |
| CN214919780U (en) | Stamping die's die carrier convenient to maintain | |
| CN109454151A (en) | Punching compound punch and hole punched device | |
| CN213245060U (en) | Stamping equipment is used in door and window production | |
| CN211679525U (en) | A multi-channel cutting device for circular forgings | |
| CN221160613U (en) | Chip-jumping-preventing die assembly | |
| CN216461057U (en) | Side flanging die stripping mechanism | |
| CN208542825U (en) | A kind of movable bending product perforating mechanism | |
| CN114147497A (en) | Automatic production device for trench cover plate | |
| CN209363374U (en) | A kind of stamping die for watch chain processing | |
| CN209697826U (en) | Blade for shredding paper stamping die | |
| KR100394116B1 (en) | An apparatus for manufacturing a sealing ring | |
| CN207592600U (en) | A kind of stamping die for terminal material belt | |
| CN221231436U (en) | Stamping device convenient for disassembling die |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |