CN115497852A - Chip automatic classification storage device - Google Patents
Chip automatic classification storage device Download PDFInfo
- Publication number
- CN115497852A CN115497852A CN202211172159.2A CN202211172159A CN115497852A CN 115497852 A CN115497852 A CN 115497852A CN 202211172159 A CN202211172159 A CN 202211172159A CN 115497852 A CN115497852 A CN 115497852A
- Authority
- CN
- China
- Prior art keywords
- tray
- clamping
- sorting
- module
- assembly
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images




Classifications
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10P—GENERIC PROCESSES OR APPARATUS FOR THE MANUFACTURE OR TREATMENT OF DEVICES COVERED BY CLASS H10
- H10P72/00—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof
- H10P72/06—Apparatus for monitoring, sorting, marking, testing or measuring
- H10P72/0611—Sorting devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/34—Sorting according to other particular properties
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10P—GENERIC PROCESSES OR APPARATUS FOR THE MANUFACTURE OR TREATMENT OF DEVICES COVERED BY CLASS H10
- H10P72/00—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof
- H10P72/30—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations
- H10P72/32—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations between different workstations
- H10P72/3202—Mechanical details, e.g. rollers or belts
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10P—GENERIC PROCESSES OR APPARATUS FOR THE MANUFACTURE OR TREATMENT OF DEVICES COVERED BY CLASS H10
- H10P72/00—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof
- H10P72/30—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations
- H10P72/32—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations between different workstations
- H10P72/3212—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations between different workstations the substrates to be conveyed not being semiconductor wafers or large planar substrates, e.g. chips or lead frames
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10P—GENERIC PROCESSES OR APPARATUS FOR THE MANUFACTURE OR TREATMENT OF DEVICES COVERED BY CLASS H10
- H10P72/00—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof
- H10P72/30—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations
- H10P72/32—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations between different workstations
- H10P72/3218—Conveying cassettes, containers or carriers
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10P—GENERIC PROCESSES OR APPARATUS FOR THE MANUFACTURE OR TREATMENT OF DEVICES COVERED BY CLASS H10
- H10P72/00—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof
- H10P72/30—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations
- H10P72/32—Handling or holding of wafers, substrates or devices during manufacture or treatment thereof for conveying, e.g. between different workstations between different workstations
- H10P72/3222—Loading to or unloading from a conveyor
Landscapes
- Specific Conveyance Elements (AREA)
Abstract
本发明公开了一种芯片自动分类存储装置,包括供料台,其顶部分类盘仓位组件、待检盘仓位组件和满盘仓位组件,供料台的底部设置料盘运送装置,在待检盘仓位组件中料盘中放置待检测的芯片,检测分类后的芯片放置在分类盘仓位组件的料盘中,当该料盘满载芯片后,料盘运送装置移动至该料盘的底部,夹持组件对料盘固定后,夹持组件松开料盘,通过料盘运送装置即可将料盘运动到预定位置,该芯片自动分类存储装置能够实现将各类料盘的转动,并且料盘的运输位于供料台的底部,避免与芯片取放装置发生运动干涉,实现了芯片在检测过程中的自动输送和存储,提高了芯片的检测效率。

The invention discloses an automatic sorting and storage device for chips, which comprises a feeding table, a sorting disk storage assembly, a disk-to-be-inspected disk storage assembly and a full disk storage assembly on the top of the feeding table. The chips to be detected are placed in the tray of the bin assembly, and the sorted chips are placed in the tray of the sorting bin bin assembly. When the tray is fully loaded with chips, the tray delivery device moves to the bottom of the tray, clamping After the component is fixed to the tray, the clamping component releases the tray, and the tray can be moved to the predetermined position through the tray conveying device. The chip automatic classification storage device can realize the rotation of various trays, and the tray's The transportation is located at the bottom of the feeding table, avoiding movement interference with the chip pick-and-place device, realizing the automatic transportation and storage of the chip during the detection process, and improving the detection efficiency of the chip.
Description
技术领域technical field
本发明涉及芯片检测设备技术领域,具体为一种芯片自动分类存储装置。The invention relates to the technical field of chip testing equipment, in particular to a chip automatic classification storage device.
背景技术Background technique
现在的电子产品、自动化工业设备及各种车辆上均安装有芯片,芯片作为设备的核心控制部件,因此芯片的需求量巨大,芯片在制作完成后,需要对芯片进行检测分类。Today's electronic products, automated industrial equipment and various vehicles are equipped with chips. Chips are the core control components of equipment, so the demand for chips is huge. After the chips are manufactured, they need to be detected and classified.
检测前将装有待检测芯片的料盘放置在料台上,并在料台上依次排布多个空料盘,用于对检测分类后的各种型号芯片进行分类储存,当料盘上的芯片满格后对该料盘进行收取,然后放置新的料盘,由于芯片根据容量分为512MB、256MB、128MB、64MB、32MB等等,因此需要反复收取以及放置新的空料盘,在放置料盘的过程中,需要暂停检测分类过程,延缓了检测效率。Before testing, place the trays containing the chips to be tested on the material table, and arrange a number of empty trays on the table in sequence to classify and store the various types of chips after detection and classification. After the chip is full, the tray is charged, and then a new tray is placed. Since the chip is divided into 512MB, 256MB, 128MB, 64MB, 32MB, etc. according to the capacity, it is necessary to repeatedly collect and place a new empty tray. In the process of feeding trays, it is necessary to suspend the detection and classification process, which delays the detection efficiency.
发明内容Contents of the invention
针对现有技术中存在的问题,本发明提供一种芯片自动分类存储装置,实现料盘的自动转运及收纳,提高了芯片的检测分类效率。Aiming at the problems existing in the prior art, the present invention provides an automatic sorting storage device for chips, which realizes the automatic transfer and storage of trays, and improves the detection and sorting efficiency of chips.
本发明是通过以下技术方案来实现:The present invention is achieved through the following technical solutions:
一种芯片自动分类存储装置,包括供料台,其顶部设置多个仓位组件,供料台的底部设置料盘运送装置;An automatic sorting and storage device for chips, comprising a feeding table, a plurality of bin components are arranged on the top of the feeding table, and a tray conveying device is arranged at the bottom of the feeding table;
所述仓位组件包括用于对料盘固定的夹持组件,以及设置在供料台顶面的料盘孔,两个夹持组件设置在供料台上并位于料盘孔的两侧,料盘设置在两个夹持组件之间,并通过两个夹持组件悬置在料盘孔的正上方;The bin assembly includes a clamping assembly for fixing the tray, and a tray hole arranged on the top surface of the feeding platform, two clamping assemblies are arranged on the feeding platform and are located on both sides of the tray hole, the feeding tray The disc is set between the two clamping components, and is suspended directly above the tray hole through the two clamping components;
所述料盘运送装置包括双向耦合直线运输装置、Z向移动模组和夹持模组;Z向移动模组设置在双向耦合直线运输装置上,夹持模组与Z向移动模组连接,双向耦合直线运输装置和Z向移动模组的移动方向结合能够使夹持模组移动至各仓位组件对应的料盘孔位置。The tray conveying device includes a two-way coupling linear conveying device, a Z-direction moving module and a clamping module; the Z-directing moving module is arranged on the two-way coupling linear conveying device, the clamping module is connected with the Z-directing moving module, The combination of the two-way coupling linear transport device and the moving direction of the Z-direction moving module can make the clamping module move to the position of the tray hole corresponding to each warehouse component.
优选的,所述仓位组件包括分类盘仓位组件、待检盘仓位组件和满盘仓位组件;Preferably, the bin assembly includes a sorting tray bin assembly, a tray bin to be inspected assembly, and a full tray bin assembly;
所述分类盘仓位组件固定的料盘中放置检测分类后的芯片,所述待检盘仓位组件固定的料盘中放置待检测的芯片,所述满盘仓位组件固定的料盘为空料盘或满芯片料盘。The chips after detection and classification are placed in the fixed tray of the sorting tray position component, the chips to be detected are placed in the fixed tray of the waiting tray position component, and the fixed tray of the full tray position component is an empty tray Or full chip tray.
优选的,所述分类盘仓位组件包括夹持座、仓位导轨、分类盘气缸和分类盘卡槽;Preferably, the sorting tray bin assembly includes a clamping seat, a bin guide rail, a sorting tray cylinder, and a sorting tray slot;
分类盘气缸设置在供料台上并位于料盘孔的边缘,夹持座与分类盘气缸的活塞连接,夹持座在分类盘气缸的带动下能够向料盘的侧壁滑动,夹持座靠近料盘的侧壁上设置有分类盘卡槽。The sorting disc cylinder is set on the feeding platform and is located at the edge of the material disc hole, the clamping seat is connected with the piston of the sorting disc cylinder, and the clamping seat can slide to the side wall of the material disc under the drive of the sorting disc cylinder, and the clamping seat A sorting tray clamping slot is arranged on the side wall close to the material tray.
优选的,所述夹持座通过导轨与供料台滑动连接。Preferably, the clamping seat is slidably connected to the feeding platform through guide rails.
优选的,所述待检盘仓位组件包括料盘导向架和待检盘夹持组件,料盘导向架设置在供料台上并位于料盘孔的边缘,多个上下叠置的料盘设置在料盘导向架中并位于料盘孔的上方,两个待检盘夹持组件对称设置在料盘孔的边缘,两个待检盘夹持组件用于最下层相邻的两个料盘进行夹持固定。Preferably, the tray position component to be inspected includes a tray guide frame and a tray clamping assembly to be inspected, the tray guide frame is arranged on the feeding platform and is located on the edge of the tray hole, and a plurality of stacked trays are arranged In the tray guide frame and above the tray hole, two tray clamping assemblies to be inspected are symmetrically arranged on the edge of the tray hole, and the two tray clamping assemblies to be inspected are used for the two adjacent trays at the bottom Perform clamping and fixing.
优选的,所述待检盘夹持组件包括上气缸、下气缸和下滑块和上滑块;Preferably, the disc clamping assembly to be inspected includes an upper cylinder, a lower cylinder, a lower slider and an upper slider;
所述上气缸和下气缸上下叠置,上气缸的活塞与上滑块连接,下滑块与下气缸的活塞连接,上滑块和下滑块靠近料盘的一侧均设置有凸起的定位台,当定位台位于料盘的顶部对料盘固定。The upper cylinder and the lower cylinder are stacked up and down, the piston of the upper cylinder is connected with the upper slider, and the lower slider is connected with the piston of the lower cylinder, and the side of the upper slider and the lower slider near the material tray is provided with a raised The positioning platform, when the positioning platform is located at the top of the tray, fixes the tray.
优选的,所述满盘仓位组件包括料盘导向架和单向夹持组件,料盘导向架设置在料盘孔的边缘,多个上下叠置的料盘设置在料盘导向架中,两个单向夹持组件对称设置在料盘孔的边缘并与料盘导向架连接,两个单向夹持组件用于最下层的料盘进行夹持固定,并且使料盘自下而上进入料盘导向架中。Preferably, the full tray position assembly includes a tray guide frame and a one-way clamping assembly, the tray guide frame is arranged on the edge of the tray hole, and a plurality of stacked trays are arranged in the tray guide frame, two Two one-way clamping components are symmetrically arranged on the edge of the tray hole and connected with the tray guide frame. Two one-way clamping components are used for clamping and fixing the bottom tray, and the tray enters from bottom to top. In the tray guide frame.
优选的,所述单向夹持组件包括支撑块,料盘导向架的一侧的下部设置有固定槽,支撑块的一端转动设置在固定槽中,支撑块的轴向并沿料盘孔的边缘平行设置,支撑块的顶部和底部分别设置有支撑面和定位面,并且支撑面和定位面平行设置,支撑面和定位面靠近料盘的一侧通过导向面连接,并且导向面倾斜设置。Preferably, the one-way clamping assembly includes a support block, a fixing groove is provided at the lower part of one side of the tray guide frame, and one end of the support block is rotatably arranged in the fixing groove, and the axial direction of the support block is along the direction of the hole of the tray. The edges are arranged in parallel, and the top and bottom of the support block are respectively provided with a support surface and a positioning surface, and the support surface and the positioning surface are arranged in parallel, and the side of the support surface and the positioning surface close to the material tray is connected by a guide surface, and the guide surface is inclined.
优选的,所述双向耦合直线运输装置包括X向移动模组、Y向移动模组;Preferably, the two-way coupled linear transport device includes an X-direction movement module and a Y-direction movement module;
所述Y向移动模组设置在X向移动模组上,并且Y向移动模组与X向移动模组的移动方向相互垂直,Z向移动模组与Y向移动模组的移动部件连接。The Y-direction mobile module is arranged on the X-direction mobile module, and the moving directions of the Y-direction mobile module and the X-direction mobile module are perpendicular to each other, and the Z-direction mobile module is connected with the moving parts of the Y-direction mobile module.
优选的,所述Z向移动模组包括偏心轴、立板、连杆、升降板和垂直导向装置;Preferably, the Z-direction moving module includes an eccentric shaft, a vertical plate, a connecting rod, a lifting plate and a vertical guide;
所述立板垂直设置在Y向移动模组的移动部件上,升降板设置在立板的一侧并通过垂直导向装置连接,偏心轴设置在立板上,连杆的上端升降板转动连接,连杆的下端与偏心轴转动连接,偏心轴与驱动电机的输出轴偏心连接,所述夹持模组设置在升降板的底部。The vertical plate is vertically arranged on the moving parts of the Y-direction moving module, the lifting plate is arranged on one side of the vertical plate and connected by a vertical guide device, the eccentric shaft is set on the vertical plate, and the lifting plate at the upper end of the connecting rod is rotatably connected. The lower end of the connecting rod is rotationally connected with the eccentric shaft, and the eccentric shaft is eccentrically connected with the output shaft of the drive motor, and the clamping module is arranged at the bottom of the lifting plate.
与现有技术相比,本发明具有以下有益的技术效果:Compared with the prior art, the present invention has the following beneficial technical effects:
本发明提供的一种芯片自动分类存储装置,包括供料台,其顶部分类盘仓位组件、待检盘仓位组件和满盘仓位组件,供料台的底部设置料盘运送装置,在待检盘仓位组件中料盘中放置待检测的芯片,检测分类后的芯片放置在分类盘仓位组件的料盘中,当该料盘满载芯片后,料盘运送装置移动至该料盘的底部,夹持组件对料盘固定后,夹持组件松开料盘,通过料盘运送装置即可将料盘运动到预定位置,该芯片自动分类存储装置能够实现将各类料盘的转动,例如,将空料盘运输至分类盘仓位组件中,对满载的料盘进行收回,将承载待检芯片的料盘运输至待检盘仓位组件,并且料盘的运输位于供料台的底部,避免与芯片取放装置发生运动干涉,实现了芯片在检测过程中的自动输送和存储,提高了芯片的检测效率。The invention provides an automatic sorting and storage device for chips, which includes a feeding table, a sorting tray storage assembly on the top, a disk storage assembly to be inspected, and a full disk storage assembly. The bottom of the feeding table is provided with a tray transport device. The chips to be detected are placed in the tray of the bin assembly, and the sorted chips are placed in the tray of the sorting bin bin assembly. When the tray is fully loaded with chips, the tray delivery device moves to the bottom of the tray, clamping After the component is fixed to the tray, the clamping component releases the tray, and the tray can be moved to the predetermined position through the tray conveying device. The chip automatic classification storage device can realize the rotation of various trays, for example, the empty The trays are transported to the sorting tray assembly, and the full trays are recovered, and the trays carrying the chips to be inspected are transported to the tray assembly to be inspected, and the trays are transported at the bottom of the feeding table to avoid contact with the chips. The movement interference of the release device realizes the automatic transportation and storage of the chip during the detection process, and improves the detection efficiency of the chip.
附图说明Description of drawings
图1为本发明全自动芯片检测分拣系统的外观图示意图;Fig. 1 is a schematic diagram of the appearance of the automatic chip detection and sorting system of the present invention;
图2为本发明全自动芯片检测分拣系统的结构图;Fig. 2 is a structural diagram of the automatic chip detection and sorting system of the present invention;
图3为本发明料芯片自动分类存储装置的结构示意图;Fig. 3 is a structural schematic diagram of an automatic classification storage device for material chips of the present invention;
图4为本发明料芯片自动分类存储装置的仓位布置示意图;Fig. 4 is a schematic diagram of the position layout of the automatic classification storage device for material chips of the present invention;
图5为本发明供料台的结构示意图;Fig. 5 is a schematic structural view of the feeding platform of the present invention;
图6为本发明分类盘仓位组件的结构示意图;Fig. 6 is a structural schematic diagram of the classification tray bin assembly of the present invention;
图7为本发明分类盘仓位组件的夹持组件的结构示意图;Fig. 7 is a structural schematic diagram of the clamping assembly of the sorting tray bin assembly of the present invention;
图8为本发明待检盘仓位组件的结构示意图;Fig. 8 is a schematic structural view of the disk storage unit to be inspected according to the present invention;
图9为本发明待检盘的夹持组件的结构示意图;9 is a schematic structural view of the clamping assembly of the disk to be inspected in the present invention;
图10为本发明满盘仓位组件的结构示意图;Fig. 10 is a schematic structural view of the full-disk storage unit of the present invention;
图11为本发明满盘仓位组件的夹持组件的结构示意图;Fig. 11 is a schematic structural view of the clamping assembly of the full tray storage assembly of the present invention;
图12为本发明料盘运送装置的结构示意图;Fig. 12 is a schematic structural view of the tray conveying device of the present invention;
图13为本发明料盘运送装置的局部结构图;Fig. 13 is a partial structural diagram of the tray conveying device of the present invention;
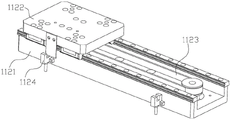
图14为本发明料盘运送装置的Y向移动装置的结构示意图;Fig. 14 is a structural schematic diagram of the Y-direction moving device of the tray conveying device of the present invention;
图15为本发明料盘运送装置的Y向移动装置的内部结构示意图;15 is a schematic diagram of the internal structure of the Y-direction moving device of the tray conveying device of the present invention;
图16为本发明料盘运送装置的Z向移动装置的结构示意图;Fig. 16 is a structural schematic diagram of the Z-direction moving device of the tray conveying device of the present invention;
图17为本发明料盘运送装置的Z向移动装置的内部结构示意图;17 is a schematic diagram of the internal structure of the Z-direction moving device of the tray conveying device of the present invention;
图中:1、芯片自动分类存储装置;2、芯片取放装置;3、芯片位置校准装置;4、检测装置;10、供料台;11、料盘运送装置;12、料盘仓位模组;100、料盘;111、X向移动模组;112、Y向移动模组;113、Z向移动模组;114、夹持模组;121,分类盘仓位组件;122,检测盘仓位组件;123,待检盘仓位组件;124,满盘仓位组件;125,空盘仓位组件;1121、Y向基座;1122、固定座;1123、驱动装置;1124、行程开关;1125、滑块;1126、连接座;1127、主动轮;1128、从动轮;1131、基板;1132、垂直导轨;1133、偏心轴;1134、立板;1135、驱动电机;1136、连杆;1137、T型滑块;1138、升降板;1211,夹持座;1212,仓位导轨;1213,分类盘气缸;1214,分类盘卡槽;1231,导料柱;1232,上气缸;1233,下气缸;1234,导向座;1235,下滑块;1236,下滑块;1241,支撑架;1242,支撑块;1243,导向面;1244,定位柱;1245,定位面;1246,支撑面。In the figure: 1. Chip automatic sorting storage device; 2. Chip pick and place device; 3. Chip position calibration device; 4. Detection device; 10. Feeding platform; ;100, material tray; 111, X-direction moving module; 112, Y-direction moving module; 113, Z-direction moving module; 114, clamping module; ; 123, the disk storage component to be checked; 124, the full disk storage component; 125, the empty disk storage component; 1121, the Y-direction base; 1122, the fixed seat; 1126, connecting seat; 1127, driving wheel; 1128, driven wheel; 1131, base plate; 1132, vertical guide rail; 1133, eccentric shaft; 1134, vertical plate; 1135, drive motor; 1136, connecting rod; ;1138, lifting plate; 1211, clamping seat; 1212, position guide rail; 1213, sorting disc cylinder; 1214, sorting disc slot; 1231, guide column; 1232, upper cylinder; 1235, the lower slider; 1236, the lower slider; 1241, the support frame; 1242, the support block; 1243, the guide surface;
具体实施方式detailed description
下面结合附图对本发明做进一步的详细说明,所述是对本发明的解释而不是限定。The present invention will be further described in detail below in conjunction with the accompanying drawings, which are explanations rather than limitations of the present invention.
参阅图1和2,本发明提供的芯片自动分类存储装置应用于芯片的检测分拣系统中,该芯片检测分拣系统,包括无尘仓,以及设置在其内部的芯片自动分类存储装置1、芯片取放装置2、芯片位置校准装置3和检测装置4;芯片取放装置2设置在芯片自动分类存储装置的一侧,芯片取放装置2包括多向耦合输送装置以及与其连接的真空笔,多向耦合输送装置与真空笔配合,将芯片自动分类存储装置1上的待检芯片输送至检测装置4,检测装置用于检测芯片的容量,并通过芯片取放装置2将其放置在芯片自动分类存储装置1对应的料盘中,芯片位置校准装置3用于对芯片的位置定位,将芯片精确放置在检查装置上。Referring to Figures 1 and 2, the chip automatic sorting storage device provided by the present invention is applied in a chip detection and sorting system. The chip detection and sorting system includes a dust-free bin, and an automatic chip sorting storage device 1, A chip pick-and-place device 2, a chip position calibration device 3, and a detection device 4; the chip pick-and-place device 2 is arranged on one side of the chip automatic classification storage device, and the chip pick-and-place device 2 includes a multi-directional coupling conveying device and a vacuum pen connected thereto, The multi-directional coupling conveying device cooperates with the vacuum pen to transport the chips to be inspected on the chip automatic classification storage device 1 to the detection device 4. The detection device is used to detect the capacity of the chip and place it on the chip automatic sorting device 2 through the chip pick-and-place device 2. In the tray corresponding to the classification storage device 1 , the chip position calibration device 3 is used to position the chip and accurately place the chip on the inspection device.
参阅图3-17,一种芯片自动分类存储装置1包括供料台10、料盘运送装置11和料盘仓位模组12;料盘仓位模组12设置在供料台10的顶部,料盘仓位模组12用于对各类料盘分类放置,料盘运送装置11设置在供料台10的底部,料盘运送装置11用于将各类料盘运输至料盘仓位模组12的对应位置;Referring to Fig. 3-17, an automatic chip sorting storage device 1 includes a feeding table 10, a
所述料盘仓位模组12包括分类盘仓位组件121、检测盘仓位组件122、待检盘仓位组件123、满盘仓位组件124和空盘仓位组件125;The tray storage module 12 includes a
分类盘仓位组件121用于存放分类后芯片,检测盘仓位组件122用于存放当前检测的芯片,待检盘仓位组件123用于存放待检测的芯片,满盘仓位组件124用于存放分类后的芯片组,空盘仓位组件125用于存放空置的料盘100。The sorting
所述分类盘仓位组件121包括料盘和分类盘夹持组件,所述供料台10的顶面设置有料盘孔,两个分类盘夹持组件设置在供料台上并位于料盘孔的两侧,料盘设置在两个分类盘夹持组件之间,并通过两个分类盘夹持组件悬置在料盘孔的正上方。The classification
所述分类盘夹持组件包括夹持座1211、仓位导轨1212、分类盘气缸1213和分类盘卡槽1214;分类盘气缸1213设置在供料台上并位于料盘孔的边缘,夹持座1211与分类盘气缸1213的活塞连接,分类盘气缸1213的底部设置有滑槽,仓位导轨1212设置在供料台上并与滑槽配合,夹持座1211在分类盘气缸1213的带动下能够沿仓位导轨1212向料盘的侧壁滑动,夹持座1211靠近料盘的侧壁上设置有分类盘卡槽1214,分类盘卡槽1214能够卡接在料盘的边缘,两个分类盘夹持组件的夹持座1211相对运动实现对料盘的固定,当两个分类盘夹持组件的夹持座1211相背运动接触对料盘的夹持,料盘能够自料盘孔被料盘运送装置运输。The classification disc clamping assembly includes a clamping
分类盘夹持组件的工作原理如下:The sorting tray clamping assembly works as follows:
料盘上整列设置有多个独立的芯片固定腔,例如,该料盘上用于存储容量为512M的芯片,当料盘上所有芯片固定腔中均放置512M的芯片后,料盘运送装置移动至该料盘孔的下方,并对该料盘承托,此时两个分类盘夹持组件相背运动解除对料盘的锁定,通过料盘运送装置11将该料盘输送至满盘仓位组件124,然后料盘运送装置11再将空盘仓位组件中的空料盘运输至该分类盘仓位组件中,并将空料盘顶升至预定高度,分类盘夹持组件对该空料盘进行夹持固定。There are multiple independent chip fixing cavities arranged on the tray. For example, the tray is used to store chips with a capacity of 512M. After all the chip fixing cavities on the tray are placed with 512M chips, the tray delivery device will move To the bottom of the tray hole, and support the tray, at this time, the two sorting tray clamping components move in opposite directions to release the locking of the tray, and the tray is transported to the full tray position by the
待检盘仓位组件123包括料盘导向架和待检盘夹持组件,供料台上设置有料盘孔,料盘导向架设置在供料台上并位于料盘孔的边缘,多个上下叠置的料盘设置在料盘导向架中并位于料盘孔的上方,两个待检盘夹持组件对称设置在料盘孔的边缘,两个待检盘夹持组件用于最下层相邻的两个料盘进行夹持固定。The
所述料盘导向架包括两个对称设置的导料柱1231,两个导料柱1231沿料盘孔的对角设置,导料柱1231上设置有卡槽,该卡槽与料盘的顶角配合,所述卡槽为直角槽,多个料盘位于两个导料柱之间,该料盘上设置有待检芯片。The material tray guide frame includes two symmetrically arranged
所述待检盘夹持组件包括上气缸1232、下气缸1233、导向座1234、下滑块1235和上滑块1236。The disc clamping assembly to be inspected includes an
所述上气缸1232和下气缸1233上下叠置,下气缸1233固定在供料台上并位于料盘孔的边缘,上气缸1232的活塞与上滑块1236连接,下滑块1235与下气缸1233的活塞连接,上滑块1236位于下滑块1235的顶部,上滑块1236和下滑块1235的两侧设置有导向座1234,导向座1234上设置有与上滑块1236和下滑块1235侧壁配合滑槽,用于对上滑块1236和下滑块1235的运动方向导向,上滑块1236和下滑块1235靠近料盘的一侧均设置有凸起的定位台,当定位台位于料盘的顶部,实现对料盘的固定。The
待检盘仓位组件123的工作原理如下:The operating principle of the
初始状态下,上气缸1232和下气缸1233的活塞伸出,使上滑块1236和下滑块1235的定位台位于最下层两个料盘的顶部,通过两组待检盘夹持组件对两个料盘进行固定,当需要对最下层的料盘的芯片检测时,将料盘运送装置11移动自该料盘的底部并接触,然后两个下气缸的活塞缩回,该料盘在重力作用下压在料盘运送装置11上,将其移动至检测盘仓位组件位置,当最下层料盘移走后,下气缸1233的活塞复位,然后上气缸的活塞缩回,在重力作用下当前最下层的料盘落在下气缸的下滑块1235的定位台上。In the initial state, the pistons of the
所述满盘仓位组件124包括料盘导向架和单向夹持组件,供料台上设置有料盘孔,料盘导向架设置在供料台上并位于料盘孔的边缘,多个上下叠置的料盘设置在料盘导向架中并位于料盘孔的上方,两个单向夹持组件对称设置在料盘孔的边缘并与料盘导向架连接,两个单向夹持组件用于最下层的料盘进行夹持固定,并且使料盘自下而上进入料盘导向架中。The full
所述料盘导向架包括两个对称设置的支撑架1241,两个支撑架1241沿料盘孔的对角设置,支撑架1241上设置有卡槽,该卡槽与料盘的顶角配合,所述卡槽为直角槽,多个料盘位于两个导料柱之间,该料盘上设置有检测后的同一型号的芯片。The tray guide frame includes two symmetrically arranged
所述单向夹持组件包括支撑块1242和定位柱1244,支撑块1242的一侧设置有固定槽,支撑架1241的一端转动设置在固定槽中,支撑块1242并沿料盘孔的边缘平行设置,定位柱1244设置在固定槽中并位于支撑块1242的顶部,支撑块1242的顶部和底部分别设置有支撑面1246和定位面1245,并且支撑面1246和定位面1245平行设置,支撑面1246和定位面1245靠近料盘的一侧通过导向面1243连接,并且导向面1243倾斜设置,支撑面1246和定位面1245远离料盘的一侧通过圆弧面连接。The one-way clamping assembly includes a
当对料盘支撑时,支撑面水平设置在料盘的底部,并且定位面与固定槽的底面抵接,使支撑面始终保持在水平状态,当料盘进入满盘仓位组件124中时,料盘运送装置将料盘移动至料盘孔中并向上顶升,料盘的边缘对导向面实现推力使导向块转动,当导向面处于垂直状态时,此时,支撑面与定位柱抵接,避免支撑块过渡旋转,料盘自下而上进入料盘导向架中,当料盘的侧壁与导向面分离,支撑块复位支撑面处于水平状态,料盘下落支撑块对料盘支撑固定。When supporting the material tray, the support surface is horizontally arranged on the bottom of the material tray, and the positioning surface abuts against the bottom surface of the fixed groove, so that the support surface remains in a horizontal state all the time. When the material tray enters the full
在本实施例中,包括三个分类盘仓位组件121、一个检测盘仓位组件122,三个满盘仓位组件124、一个待检盘仓位组件123和一个空盘仓位组件125。In this embodiment, it includes three sorting
分类盘仓位组件121和检测盘仓位组件122的结构相同,分类盘仓位组件121中的料盘用于放置检测后的同一型号芯片,检测盘仓位组件122中的料盘上放置待检测分类的芯片,空盘仓位组件125和待检盘仓位组件123的结构相同,不同之处在于料盘的芯片的类型,空盘仓位组件125中的料盘为空料盘,待检盘仓位组件123中的料盘中放置待检测的芯片。The classification
三个分类盘仓位组件121和检测盘仓位组件122,并沿直线布置在供料台靠近芯片取放装置2的一侧,三个分类盘仓位组件分别用于存放512M、1G和4G容量的芯片,三个满盘仓位组件124、一个待检盘仓位组件123和一个空盘仓位组件125,并沿直线布置在供料台远离芯片取放装置2的一侧,并且待检盘仓位组件123和空盘仓位组件125位于供料台的两端,这样布置提高料盘的流转效率。Three sorting
料盘运送装置11设置在供料台的底部,其包括X向移动模组111、Y向移动模组112、Z向移动模组113和夹持模组114;The
所述Y向移动模组112包括Y向基座1121、固定座1122、同步带驱动装置和行程开关1124;X向移动模组111为直线驱动模组,直线驱动模组的内部设置丝杠滑块机构,电机驱动丝杆转动,丝杆带动滑座移动,直线驱动模组沿供料台的长度方向设置,Y向基座1121固定在直线驱动模组的滑座上,同步带驱动装置设置在Y向基座1121中,固定座1122设置在基座1121的顶部并与同步带驱动装置连接,同步带驱动装置带动固定座1122移动,并且移动方向与直线驱动模组的滑座移动方向相互垂直,Z向移动模组113设置在固定座1122上,夹持模组114设置在Z向移动模组113的顶部,Z向移动模组113用于带动夹持模组114上下移动。The Y-
所述同步带驱动装置包括驱动装置1123、连接座1126、主动轮1127和从动轮1128;Y向基座1121的两侧设置有向上延伸的固定板,支撑板的顶部设置有导轨,滑块1125配装在导轨上,同步带驱动装置设置在两个平行的导轨之间,主动轮1127和从动轮1128位于Y向基座1121的两端并通过同步带连接,连接座1126固定在同步带上,连接座1126与固定座1122通过螺栓连接,驱动装置1123位于Y向基座1121的底部并与主动轮连接,行程开关1124设置在Y向基座1121的一侧,用于检测固定座1122的移动位置,避免固定座1122脱离导轨,Y向基座1121的两端均设置有行程开关1124。The synchronous belt driving device includes a
工作时,同步带带动连接座1126移动,连接座1126带动固定座1122沿导轨移动,同时结合X向移动模组111,进而实现Z向移动模组113和夹持模组114的沿水平面移动。During operation, the synchronous belt drives the connecting
Z向移动模组113用于调节夹持模组114的高度,Z向移动模组113包括基板1131、偏心轴1133、立板1134、连杆1136、升降板1138和垂直导向装置;The Z-
所述基板1131固定在固定座1122的顶部,立板1134垂直设置在基板1131的顶部,升降板设置在立板的一侧并通过垂直导向装置连接,偏心轴1133设置在立板上,连杆1136的上端升降板1138转动连接,连杆1136的下端与偏心轴1133转动连接,偏心轴与驱动电机1135的输出轴偏心连接,驱动电机1135固定在立板的另一侧。The
所述垂直导向装置包括垂直导轨1132和T型滑块1137;两个垂直导轨1132间隔且平行设置在立板两侧的边缘,T型滑块1137设置在升降板的一侧,T型滑块1137与垂直导轨1132滑动连接,驱动电机1135的输出轴穿过立板位于两个垂直导轨1132之间,输出轴的端部设置有转轮,偏心轴设置在转轮的边缘,偏心轴通过轴承与连杆1136的下端连接。Described vertical guiding device comprises
工作时,驱动电机1135带动转轮旋转,转轮带动偏心轴圆周移动,同时带动连杆的下端圆周运动,并且连杆的上端上下往复移动,进而实现升降板的垂直移动。When working, the driving
所述夹持模组114设置在升降板的底部,夹持模组114上设置有两个能够同步相背或相向移动的夹头1141,夹持模组114为双向直线模组,丝杠的两端螺旋槽的旋向相反,丝杆的两端分别设置移动滑座,夹头设置在移动滑座的顶部,夹头1141的远离另一夹头的端部设置有向上延伸的卡板,当料盘位于两个夹头上,两个夹头相对移动,两个卡板能够对料盘的两个平行的侧壁夹紧固定,实现对料盘的夹持。The
该料盘运送装置将X向移动模组、Y向移动模组和Z向移动模组的运动方向耦合,实现夹持模组在平面和高度方向实现随意移动,当需要转运料盘时,通过X向移动模组和Y向移动模组将夹持模组移动至对应的料盘孔的位置,然后通过Z向移动模组使夹头位于料盘的底部,然后料盘的夹持组件打开,夹头将料盘固定后,再通过X向移动模组、Y向移动模组和Z向移动模组的配合,将料盘运输至预定位置。The tray conveying device couples the movement directions of the X-direction moving module, the Y-direction moving module and the Z-direction moving module to realize the random movement of the clamping module in the plane and height directions. The X-direction moving module and the Y-direction moving module move the clamping module to the position of the corresponding tray hole, and then move the module in the Z direction so that the chuck is located at the bottom of the tray, and then the clamping assembly of the tray is opened , After the chuck fixes the tray, the tray is transported to the predetermined position through the cooperation of the X-direction movement module, the Y-direction movement module and the Z-direction movement module.
本发明还提供的一种全自动芯片检测分拣系统,包括无尘仓,以及设置在其内部的料芯片自动分类存储装置1、芯片取放装置2、芯片位置校准装置3和检测装置4;芯片自动分类存储装置1上设置多个仓位模组,对不同状态的料盘进行分类存储,并结合料盘运送装置11对不同状态的料盘进行自动转动,所述芯片取放装置2由旋转组件、Y向移动组件和高度移动组件组成,形成三维运输平台,在该三维运输平台上设置真空笔,实现对芯片的转移,同时在三维运输平台上设置定位组件,定位组件确定芯片的位置,将待检芯片运转至检测台,以及将检测后的芯片放置料盘中,通过CCD相机获取芯片的位置,大大提高了吸取芯片的位置精度,该全自动芯片检测分拣系统实现芯片自动检测和分拣,降低了人工成本,提高了芯片的生产效率,具有较高的使用价值和推广价值。The present invention also provides a fully automatic chip detection and sorting system, including a dust-free bin, and an automatic sorting storage device 1 for material chips, a chip pick-and-place device 2, a chip position calibration device 3 and a detection device 4 arranged inside it; The chip automatic sorting storage device 1 is provided with a plurality of bin modules to classify and store the trays in different states, and automatically rotate the trays in different states in combination with the
以上内容仅为说明本发明的技术思想,不能以此限定本发明的保护范围,凡是按照本发明提出的技术思想,在技术方案基础上所做的任何改动,均落入本发明权利要求书的保护范围之内。The above content is only to illustrate the technical idea of the present invention, and cannot limit the protection scope of the present invention. Any changes made on the basis of the technical solution according to the technical idea proposed in the present invention, all fall into the scope of the claims of the present invention. within the scope of protection.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211172159.2A CN115497852A (en) | 2022-09-26 | 2022-09-26 | Chip automatic classification storage device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211172159.2A CN115497852A (en) | 2022-09-26 | 2022-09-26 | Chip automatic classification storage device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN115497852A true CN115497852A (en) | 2022-12-20 |
Family
ID=84470016
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202211172159.2A Pending CN115497852A (en) | 2022-09-26 | 2022-09-26 | Chip automatic classification storage device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115497852A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116714976A (en) * | 2023-05-31 | 2023-09-08 | 厦门微亚智能科技有限公司 | A kind of loading and unloading equipment and method to prevent downtime of the upstream and downstream of the assembly line |
-
2022
- 2022-09-26 CN CN202211172159.2A patent/CN115497852A/en active Pending
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116714976A (en) * | 2023-05-31 | 2023-09-08 | 厦门微亚智能科技有限公司 | A kind of loading and unloading equipment and method to prevent downtime of the upstream and downstream of the assembly line |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111169952B (en) | Part sorting wobble plate stacking machine | |
| CN212821225U (en) | Chip arrangement device for chip aging test | |
| CN112246663B (en) | Product counting device and chip testing equipment | |
| CN109158338B (en) | Vertical material sorting all-in-one of getting of lithium cell | |
| CN211217570U (en) | A piston testing machine | |
| CN111482374A (en) | Silicon wafer inspection and sorting machine and sorting method thereof | |
| CN112122146B (en) | Functional and appearance integrated testing equipment | |
| CN114999811B (en) | Production line of transformer coil and testing machine thereof | |
| CN214358858U (en) | Automatic feeding system | |
| CN216889070U (en) | An automatic discharge device that can stack trays | |
| CN115301574A (en) | A screening and palletizing equipment for printed circuit boards | |
| CN115709178A (en) | Full-automatic chip detection sorting system and method | |
| CN220760130U (en) | Chip sorting detector | |
| CN219581137U (en) | Automatic chip test sorter of circulation classification | |
| CN208004340U (en) | Semiconductor chilling plate integral test system | |
| CN111824764A (en) | A conveying device for chip trays | |
| CN106623001A (en) | An automatic pre-charging and testing equipment | |
| CN213934073U (en) | Circulator vector net testing machine | |
| CN213792877U (en) | Product counting device and chip testing equipment | |
| CN218619038U (en) | A position in storehouse subassembly for chip feed platform | |
| CN112024428B (en) | OCV test machine and battery | |
| CN221026290U (en) | Automatic chip classification storage device | |
| CN219842966U (en) | Material tray conveying device for chip feeding table | |
| CN222659293U (en) | Automatic piston sorting machine | |
| CN219842957U (en) | Chip classification storage device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination |