CN115295855A - Polarity detection and restoration integrated device for cell group - Google Patents
Polarity detection and restoration integrated device for cell group Download PDFInfo
- Publication number
- CN115295855A CN115295855A CN202210793828.1A CN202210793828A CN115295855A CN 115295855 A CN115295855 A CN 115295855A CN 202210793828 A CN202210793828 A CN 202210793828A CN 115295855 A CN115295855 A CN 115295855A
- Authority
- CN
- China
- Prior art keywords
- battery pack
- double
- speed chain
- repair
- tooling
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images





Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/04—Construction or manufacture in general
- H01M10/0404—Machines for assembling batteries
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01R—MEASURING ELECTRIC VARIABLES; MEASURING MAGNETIC VARIABLES
- G01R31/00—Arrangements for testing electric properties; Arrangements for locating electric faults; Arrangements for electrical testing characterised by what is being tested not provided for elsewhere
- G01R31/36—Arrangements for testing, measuring or monitoring the electrical condition of accumulators or electric batteries, e.g. capacity or state of charge [SoC]
- G01R31/385—Arrangements for measuring battery or accumulator variables
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01R—MEASURING ELECTRIC VARIABLES; MEASURING MAGNETIC VARIABLES
- G01R31/00—Arrangements for testing electric properties; Arrangements for locating electric faults; Arrangements for electrical testing characterised by what is being tested not provided for elsewhere
- G01R31/36—Arrangements for testing, measuring or monitoring the electrical condition of accumulators or electric batteries, e.g. capacity or state of charge [SoC]
- G01R31/396—Acquisition or processing of data for testing or for monitoring individual cells or groups of cells within a battery
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01R—MEASURING ELECTRIC VARIABLES; MEASURING MAGNETIC VARIABLES
- G01R31/00—Arrangements for testing electric properties; Arrangements for locating electric faults; Arrangements for electrical testing characterised by what is being tested not provided for elsewhere
- G01R31/50—Testing of electric apparatus, lines, cables or components for short-circuits, continuity, leakage current or incorrect line connections
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Secondary Cells (AREA)
- Battery Mounting, Suspending (AREA)
Abstract
Description
技术领域technical field
本发明涉及电芯加工技术领域,更具体地说,它涉及一种电芯组极性检测修复一体装置。The invention relates to the technical field of electric core processing, and more specifically, relates to an integrated device for detecting and repairing the polarity of electric core packs.
背景技术Background technique
电池模组PACK工艺是新能源电池生产过程中不可省略的生产环节,一个电池模组是由多个单体电芯的串并联连接而成,一旦在电芯串并联过程中出现错误排列,轻则造成返工带来的物料和人力浪费,重则出现打火的安全隐患;一个电池模组内会存在电芯的多种串并联排列组合。The battery module PACK process is an indispensable production link in the production process of new energy batteries. A battery module is composed of multiple single cells connected in series and parallel. It will cause material and manpower waste caused by rework, and there will be a safety hazard of ignition; there will be various series and parallel arrangements of batteries in a battery module.
现有的模组PACK车间内,在电池模组组装完毕后,由检验人员通过目检各电芯极柱颜色排列来区分电芯的极性排列顺序是否正确,但电池模组内包含的电芯数量较多,正负极柱的交错排列,密密麻麻,在生产控制上,全靠人员目检,自检以及返工。而且检测人员目检极易疲劳,在生产期间,需要配备两个以上检验员进行周期换岗,否则易出纰漏。In the existing module PACK workshop, after the battery module is assembled, inspectors visually inspect the color arrangement of the poles of each battery cell to distinguish whether the polarity sequence of the battery cells is correct, but the batteries contained in the battery module The number of cores is large, and the positive and negative poles are staggered and densely packed. In terms of production control, it all depends on personnel's visual inspection, self-inspection and rework. Moreover, inspectors are prone to fatigue in visual inspection. During the production period, more than two inspectors need to be assigned to change positions periodically, otherwise it is easy to make mistakes.
中国专利公告号CN213600861U,名称为电芯极性检测系统,该申请案公开了一种电芯极性检测系统,所述电芯极性检测系统包括:传输机构,用于放置电芯及传输电芯;设置在所述传输机构上的检测工位;检测机构,所述检测机构设置于所述检测工位处,用于检测经过所述检测工位处的电芯的极性;安装工位,所述安装工位位于所述检测工位下游,且设置在所述传输机构的一侧,其中,所述安装工位处放置有安装模块;抓取机构,所述抓取机构设置于所述安装工位处,且抓取机构设置有抓取件,抓取件用于传输机构处的电芯移至安装工位处,在安装工位将电芯安装到安装模块,或将在安装工位处的安装有电芯的安装模块移动至传输机构。该系统仅用于判断单个电芯的极性,适用于电池模组PACK进行组装时的电芯供料排序检测,无法对完成排列后的未封装电芯组进行检测。Chinese patent announcement number CN213600861U, titled battery polarity detection system, the application discloses a battery polarity detection system, the battery polarity detection system includes: a transmission mechanism for placing the battery and transmitting the battery core; a detection station arranged on the transmission mechanism; a detection mechanism, the detection mechanism is arranged at the detection station for detecting the polarity of the electric core passing through the detection station; an installation station , the installation station is located downstream of the detection station and is arranged on one side of the transmission mechanism, wherein an installation module is placed at the installation station; a grabbing mechanism, the grabbing mechanism is arranged on the The above-mentioned installation station, and the grabbing mechanism is provided with grabbing parts, the grabbing parts are used to move the batteries at the transmission mechanism to the installation station, and the batteries are installed to the installation module at the installation station, or will be installed at the installation station. The installation module installed with the battery cell at the station moves to the transmission mechanism. The system is only used to judge the polarity of a single battery cell, and is suitable for battery cell supply sorting detection when the battery module PACK is assembled, and cannot detect the unpackaged battery pack after the arrangement is completed.
中国专利公告号CN206710521U,名称为一种新型模组电池极性检测装置,该申请公开了一种新型模组电池极性检测装置,包括电芯模组和定位机构,芯模组由独立的单体电芯组成,定位机构中固定安装有推动探针机构和探针,推动探针机构推动探针与单体电芯的电极电性连接,形成闭合测试电路,闭合测试电路中还固定安装有一号二极管、二号二极管、KA、绿灯和红灯。本实用新型的新型模组电池极性检测装置,通过设置的二极管、绿灯和红灯,由于二极管的正向导通、反向截止的单向导电特性就可以判断单体电芯的正负极性,如果排列方向正确则绿灯亮,如果排列方向错误则红灯亮,以此可以提醒作业人员模组装配是否正确。在检测到电芯组排列方向错误后,该装置是在检测装置进行修复的,这种方式存在一定的安全隐患,而通过倍速链向另一修复工位输送则会使得装置之间的连接和控制过于复杂。Chinese patent announcement number CN206710521U, titled a new type of module battery polarity detection device, the application discloses a new type of module battery polarity detection device, including a cell module and a positioning mechanism, the core module consists of an independent unit The positioning mechanism is fixedly equipped with a push probe mechanism and a probe, and the push probe mechanism pushes the probe to electrically connect with the electrodes of the single cell to form a closed test circuit. A closed test circuit is also fixedly installed in the closed test circuit. Diode No. 2, Diode No. 2, KA, Green Light and Red Light. The new module battery polarity detection device of the utility model can judge the positive and negative polarity of a single battery cell due to the one-way conduction characteristics of the forward conduction and reverse cut-off of the diode through the set diode, green light and red light. , if the arrangement direction is correct, the green light will be on, and if the arrangement direction is wrong, the red light will be on, so as to remind the operator whether the module assembly is correct. After detecting that the direction of the cell group is wrongly arranged, the device is repaired in the detection device. This method has certain potential safety hazards, and the transmission to another repair station through the double-speed chain will make the connection and repair between the devices difficult. Controls are too complex.
综上,本申请旨在实现一种可以缩短检测部件和修复部件之间距离,简化控制的一种电芯组极性检测修复一体装置。To sum up, the present application aims to realize an integrated battery pack polarity detection and repair device that can shorten the distance between the detection component and the repair component and simplify control.
发明内容Contents of the invention
本发明克服了上述不足,提供了一种电芯组极性检测修复一体装置,它实现了检测工位和修复工位的分离,同时设计了较短的输送方式,使得输送的控制部分简化。The present invention overcomes the above-mentioned shortcomings and provides an integrated device for detecting and repairing the polarity of the battery pack, which realizes the separation of the detection station and the repair station, and at the same time designs a shorter delivery mode to simplify the control part of the delivery.
为了解决上述技术问题,本发明采用以下技术方案:In order to solve the above technical problems, the present invention adopts the following technical solutions:
一种电芯组极性检测修复一体装置,包括An integrated device for detecting and repairing the polarity of a battery pack, comprising
倍速链,用于移动电芯组;Double speed chain, used to move the battery pack;
极性检测组件,极性检测组件上设有若干用于接触电芯组极柱的探针,探针用于获取电芯组状态;Polarity detection component, the polarity detection component is equipped with a number of probes for contacting the poles of the battery pack, and the probes are used to obtain the state of the battery pack;
修复台,用于修复电芯组;A repair station for repairing the cell pack;
和顶升平移机构;and jacking translation mechanism;
其中,修复台位于倍速链宽度方向的一侧,修复台和顶升平移机构配合在倍速链和修复台之间移动电芯组,倍速链包括上层倍速链和下层倍速链以及装载在上层倍速链或下层倍速链上的回流工装板,所述电芯组置于上层倍速链的回流工装板上,顶升平移机构包括用于移动上层倍速链上的回流工装板的上层顶升平移机构和用于移动下层倍速链上的下层顶升平移机构,修复台和上层顶升平移机构配合在上层倍速链和修复台之间移动承载电芯组的回流工装板,修复台和下层顶升平移机构配合在下层倍速链和修复台之间移动空置的回流安装板。Among them, the repair table is located on one side of the double-speed chain width direction, and the repair table and the jacking translation mechanism cooperate to move the battery pack between the double-speed chain and the repair table. The double-speed chain includes the upper double-speed chain and the lower double-speed chain Or the reflow tooling plate on the lower double-speed chain, the battery pack is placed on the reflow tooling plate of the upper double-speed chain, and the jacking and translation mechanism includes an upper jacking and translation mechanism for moving the backflow tooling plate on the upper double-speed chain and a To move the lower lifting and translation mechanism on the lower double-speed chain, the repair table and the upper lifting and translation mechanism cooperate to move the reflow tooling plate carrying the battery pack between the upper double-speed chain and the repair table, and the repair table cooperates with the lower jacking and translation mechanism Move the empty reflow mounting plate between the lower double-speed chain and the repair station.
在本申请中,整个流程包括:倍速链将电芯组输送到极性检测组件的检测位置;极性检测组件上的探针与电芯组的极柱进行接触,然后进行检测,获取电芯组的状态并传回控制器中,控制器获取电芯组的状态根据预设条件将其通过倍速链向下一流程输送或通过顶升平移机构配合修复台将电芯组输送至修复台进行修复,待修复完成后再将电芯组输送回。本装置对电芯组中的电芯逐一测量,判断其顺序,无需人工肉眼判断,精度更高,物料的报废几率更小,也更为节省人工。上层倍速链和下层倍速链的输送方向相反,上层倍速链将电芯组和回流工装板向下游工序位置输送,下层倍速链将从下游倍速链返回的回流工装板反向送回锂电池电芯组极性快速检测装置的上游,省去人工搬回回流工装板的人工。将送料倍速链和回流倍速链上下设置,节约了空间。顶升平移机构包括升降结构和平移结构,升降结构将回流工装板顶出倍速链的导槽,平移结构将回流工装板平移。修复台配合进行接收,将回流工装板移动至修复台。若电芯组无法进行修复,在移除电芯组后,将空置的回流工装板平移至下层顶升平移机构,然后下层顶升平移机构复位,由下层倍速链将空置的回流工装板送回。通过在左右方向上利用平移和升降实现了检测工位和修复工位的分离,在检测工位和修复工位之间的移动以简单的形式实现,降低了控制的复杂程度。In this application, the entire process includes: the double-speed chain transports the battery pack to the detection position of the polarity detection component; the probe on the polarity detection component contacts the pole of the battery pack, and then detects and obtains the battery The state of the group is sent back to the controller, and the controller obtains the state of the cell group and transmits it to the next process through the double-speed chain or through the jacking and translation mechanism to cooperate with the repair station to transport the cell group to the repair station according to the preset conditions. After the repair, the battery pack will be transported back after the repair is completed. The device measures the batteries in the battery pack one by one, and judges their sequence without the need for manual judgment with the naked eye. The accuracy is higher, the probability of scrapping materials is smaller, and it saves labor. The conveying directions of the upper double-speed chain and the lower double-speed chain are opposite. The upper double-speed chain transports the cell pack and the return tooling plate to the downstream process position, and the lower double-speed chain reversely sends the return tooling plate returned from the downstream double-speed chain back to the lithium battery cell. The upstream of the group polarity rapid detection device saves the labor of manually moving back to the return tooling board. The feeding double-speed chain and the return double-speed chain are set up and down, which saves space. The lifting translation mechanism includes a lifting structure and a translation structure. The lifting structure pushes the return tooling plate out of the guide groove of the double-speed chain, and the translation structure moves the return tooling plate in translation. The repair station cooperates to receive and move the reflow tooling board to the repair station. If the cell pack cannot be repaired, after removing the cell pack, move the vacant reflow tooling board to the lower jacking translation mechanism, and then reset the lower jacking translation mechanism, and send the vacant backflow tooling board back by the lower double speed chain . The separation of the detection station and the repair station is realized by using translation and lifting in the left and right directions, and the movement between the detection station and the repair station is realized in a simple form, which reduces the complexity of control.
作为优选,极性检测组件包括固定架、驱动器、安装架和探针工装板,驱动器驱动安装架相对固定架升降运动,探针工装板可拆卸连接在安装架上。锂电池电芯组极性快速检测装置包括机架,极性检测组件位于倍速链的一侧,极性检测组件固定连接在机架上,具体的,固定架固定连接在机架上。安装架固定连接驱动器的伸缩端,具体的,驱动器为伸缩电机,固定架上具有沿高度方向设置的导轨,安装架通过导轨的导向相对固定架上下升降并带动以可拆卸连接的方式连接在安装架上的探针工装板进行升降。探针工装板的竖向投影位于倍速链上。通过上述结构,实现探针工装板上的探针与到位的电芯组上的极柱接触。Preferably, the polarity detection assembly includes a fixed frame, a driver, a mounting frame and a probe tooling plate, the driver drives the mounting frame to move up and down relative to the fixed frame, and the probe tooling plate is detachably connected to the mounting frame. The lithium battery cell pack polarity rapid detection device includes a frame, the polarity detection component is located on one side of the double speed chain, the polarity detection component is fixedly connected to the frame, specifically, the fixed frame is fixedly connected to the frame. The mounting frame is fixedly connected to the telescopic end of the driver. Specifically, the driver is a telescopic motor, and the mounting frame has guide rails arranged along the height direction. The probe tooling plate on the rack is lifted. The vertical projection of the probe tooling plate is located on the double speed chain. Through the above structure, the contact between the probes on the probe tooling board and the poles on the battery pack in place is realized.
作为优选,安装架包括工装滑槽,探针工装板插入到工装滑槽中,探针工装板可拆卸连接工装滑槽,采用插入形式操作简单,便于快速更换探针工装板。Preferably, the installation frame includes a tooling chute, the probe tooling plate is inserted into the tooling chute, the probe tooling plate is detachably connected to the tooling chute, and the inserting form is easy to operate and facilitates quick replacement of the probe tooling plate.
作为优选,探针工装板上具有若干探针单元,探针单元设有对应电芯的正负极柱的探针,根据电芯组中的相邻极柱在长度和宽度方向的排列间距,探针单元进行对应阵列排布。一探针单元上固定连接有两探针,两探针之间的距离与需要检测的电芯组中的电芯上的极柱之间的距离相同。与电芯在电芯组中的排列的,探针单元也在探针工装板上对应排列。通过上述特征,使得各个探针与各个极柱之间均可以做到同时接触,避免由于虚接造成的检测错误。As a preference, there are several probe units on the probe tooling board, and the probe units are provided with probes corresponding to the positive and negative poles of the batteries. According to the arrangement spacing of the adjacent poles in the battery pack in the length and width directions, The probe units are arranged in corresponding arrays. Two probes are fixedly connected to a probe unit, and the distance between the two probes is the same as the distance between the poles on the battery cells in the battery pack to be tested. In line with the arrangement of the batteries in the battery pack, the probe units are also arranged on the probe tooling board. Through the above features, simultaneous contact between each probe and each pole can be achieved, and detection errors caused by virtual connections can be avoided.
作为优选,沿着探针工装板板面的垂向方向,工装滑槽安装有用于手拧的蝶形螺丝,操作者可以做到免工具拧转蝶形螺丝,使蝶形螺丝在工装滑槽上沿探针工装板板面的垂向方向进给从而抵接在探针工装板上,限制其上下位置。As a preference, along the vertical direction of the probe tooling board, the tooling chute is equipped with thumb screws for hand-tightening, and the operator can turn the thumb screws without tools, so that the thumb screws are in the tooling chute The upper part is fed along the vertical direction of the surface of the probe tooling board so as to abut against the probe tooling board to limit its up and down position.
作为优选,工装滑槽设有用于指示定位探针工装板到位的侧边挡块,侧边挡块可调节连接在工装滑槽上。根据不同极柱间距的电芯组,可以更换对应的探针工装板,调整侧边挡块的位置以使得探针与极柱对齐。Preferably, the tooling chute is provided with a side stopper for indicating that the tooling plate of the positioning probe is in place, and the side stopper is adjustable and connected to the tooling chute. According to the cell pack with different pole spacing, the corresponding probe tooling plate can be replaced, and the position of the side stopper can be adjusted to align the probe with the pole.
作为优选,修复台包括剃废升降机和连接在剃废升降机上的剃废架,剃废架上设有平移电机和沿倍速链宽度方向设置的平移链。剃废升降机作为修复台的一部分,起到对接顶升平移机构和提供操作平台的作用。Preferably, the repair station includes a shaving waste lifter and a shaving waste frame connected to the shaving waste lifter, and the shaving waste frame is provided with a translation motor and a translation chain arranged along the width direction of the double-speed chain. As a part of the restoration platform, the shaving waste lifter plays the role of docking the jacking translation mechanism and providing an operating platform.
作为优选,还包括用于识别电芯组的扫码器。扫码器扫描电芯组上的识别码,将识别到的编号和对应的电芯组状态绑定,在修复台进行修复时提供电芯组的状态信息,加快找到错误靶点,实现快速修复。Preferably, a code scanner for identifying the battery pack is also included. The code scanner scans the identification code on the battery pack, binds the identified number with the corresponding battery pack status, and provides the status information of the battery pack when repairing on the repair station, so as to speed up finding the wrong target and realize quick repair .
作为优选,上层倍速链上设有挡位工装,挡位工装包括挡位电机和挡位电机伸缩端的挡位块,所述挡位块为柔性材质。挡位工装用于在长度方向限制回流工装板的移动,在倍速链输送电芯组的过程中对回流工装板进行限位停下回流工装板。Preferably, gear tooling is provided on the upper double-speed chain, and the gear tooling includes a gear motor and a gear block at the telescopic end of the gear motor, and the gear block is made of a flexible material. The gear tool is used to limit the movement of the return tooling plate in the length direction, and limit the return tooling plate to stop the return tooling plate during the process of the double-speed chain conveying the battery pack.
与现有技术相比,本发明的有益效果是:Compared with prior art, the beneficial effect of the present invention is:
本装置对电芯组中的电芯逐一测量,判断其顺序,无需人工肉眼判断,精度更高,物料的报废几率更小,也更为节省人工;修复台位于倍速链的一侧,通过修复台和顶升平移机构配合实现对电芯组的转移,移动结构的形式简单,控制流程易于实现。This device measures the battery cells in the battery pack one by one, and judges their order without manual judgment with the naked eye. It has higher precision, less chance of scrapping materials, and saves labor. The repair station is located on the side of the double-speed chain. The transfer of the battery pack is realized by the cooperation of the platform and the jacking and translation mechanism. The form of the moving structure is simple, and the control process is easy to realize.
附图说明Description of drawings
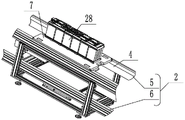
图1是本发明的结构示意图;Fig. 1 is a structural representation of the present invention;
图2是本发明的结构主视图;Fig. 2 is a structural front view of the present invention;
图3是本发明的倍速链的示意图;Fig. 3 is the schematic diagram of the double speed chain of the present invention;
图4是本发明的极性检测组件的示意图;Fig. 4 is the schematic diagram of the polarity detecting assembly of the present invention;
图5是本发明的仅装载一探针单元的探针工装板;Fig. 5 is the probe tooling board of the present invention that only loads a probe unit;
图6是本发明另一种实施例的探针工装板的结构示意图;Fig. 6 is a schematic structural view of a probe tooling board according to another embodiment of the present invention;
图7是本发明的工装滑槽的示意图;Fig. 7 is the schematic diagram of the frock chute of the present invention;
图8是本发明的剃废升降机和剃废架的结构示意图;Fig. 8 is a schematic structural view of the shaving waste elevator and the shaving waste frame of the present invention;
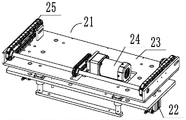
图9是本发明的顶升平移机构一个方向的立体图;Fig. 9 is a perspective view in one direction of the jacking translation mechanism of the present invention;
图10是本发明的顶升平移机构另一个方向的立体图;Fig. 10 is a perspective view in another direction of the jacking translation mechanism of the present invention;
图中:In the picture:
机架1、倍速链2、倍速链型材4、上层倍速链5、下层倍速链6、回流工装板7、极性检测组件8、固定架9、驱动器10、安装架11、工装滑槽12、侧边挡块13、标记卡14、探针工装板15、探针单元16、修复台17、剃废升降机18、剃废架19、屏幕20、顶升平移机构21、升降电机22、升降台23、平移电机24、平移链25、上层顶升平移机构26、下层顶升平移机构27、电芯组28、导向柱29、弹簧30、接触簧片31、电流传感器32、磁环33。
具体实施方式Detailed ways
下面结合附图与实施例对本公开作进一步说明。The present disclosure will be further described below in conjunction with the accompanying drawings and embodiments.
应该指出,以下详细说明都是例示性的,旨在对本申请提供进一步的说明。除非另有指明,本文使用的所有技术和科学术语具有与本申请所属技术领域的普通技术人员通常理解的相同含义。It should be pointed out that the following detailed description is exemplary and intended to provide further explanation to the present application. Unless defined otherwise, all technical and scientific terms used herein have the same meaning as commonly understood by one of ordinary skill in the art to which this application belongs.
需要注意的是,这里所使用的术语仅是为了描述具体实施方式,而非意图限制根据本申请的示例性实施方式。如在这里所使用的,除非上下文另外明确指出,否则单数形式也意图包括复数形式,此外,还应当理解的是,当在本说明书中使用术语“包含”和/或“包括”时,其指明存在特征、步骤、操作、器件、组件和/或它们的组合。It should be noted that the terminology used here is only for describing specific implementations, and is not intended to limit the exemplary implementations according to the present application. As used herein, unless the context clearly dictates otherwise, the singular is intended to include the plural, and it should also be understood that when the terms "comprising" and/or "comprising" are used in this specification, they mean There are features, steps, operations, means, components and/or combinations thereof.
在本公开中,术语如“上”、“下”、“左”、“右”、“前”、“后”、“竖直”、“水平”、“侧”、“底”等指示的方位或位置关系为基于附图所示的方位或位置关系,只是为了便于叙述本公开各部件或元件结构关系而确定的关系词,并非特指本公开中任一部件或元件,不能理解为对本公开的限制。In this disclosure, terms such as "upper", "lower", "left", "right", "front", "rear", "vertical", "horizontal", "side", "bottom" etc. refer to The orientation or positional relationship is based on the orientation or positional relationship shown in the drawings, and is only a relative term determined for the convenience of describing the structural relationship between the components or elements of the present disclosure. Public restrictions.
本公开中,术语如“固接”、“相连”、“连接”等应做广义理解,表示可以是固定连接,也可以是一体地连接或可拆卸连接;可以是直接相连,也可以通过中间媒介间接相连。对于本领域的相关科研或技术人员,可以根据具体情况确定上述术语在本公开中的具体含义,不能理解为对本公开的限制。In this disclosure, terms such as "fixed", "connected", and "connected" should be interpreted in a broad sense, which means that they can be fixedly connected, integrally connected or detachably connected; they can be connected directly or through an intermediate connection. The medium is indirectly connected. For relevant researchers or technicians in the field, the specific meanings of the above terms in the present disclosure can be determined according to specific situations, and should not be construed as limitations on the present disclosure.
实施例:Example:
一种锂电池电芯组28极性检测修复装置,如图1、2所示,包括机架1、倍速链2、极性检测组件8、修复台17和顶升平移机构21。机架1修复台17位于倍速链2宽度方向的一侧。修复台17和倍速链2位于机架1左右方向的两侧。倍速链2包括倍速链本体3、倍速链型材4、主动轴、从动轴和对应的电动机。电动机的动力输出端与倍速链本体3传动连接,两条倍速链本体3通过主动轴和从动轴传动连接,如此实现倍速链本体3的同步运动。在本实施例中,倍速链2还包括有挡位工装,挡位工装包括挡位电机和挡位电机伸缩端上的挡位块。倍速链2的结构为本领域的常规技术手段,本申请不在此赘述。A lithium
在一些实施例中,还包括用于识别电芯组28的扫码器和到位传感器。扫码器扫描电芯组28上的识别码,将识别到的编号和对应的电芯组28状态绑定,在修复台17进行修复时提供电芯组28的状态信息,加快找到错误靶点,实现快速修复。扫码器同时也用于识别电芯组28的具体型号,屏蔽极性检测组件8上的多余探针,只对与极柱接触的探针进行检测,从而实现快速检测。在一些实施例中,到位传感器为光电传感器,当电芯组28运动至阻挡光电传感器的光路时,扫码器开始工作。In some embodiments, a code scanner and an in-position sensor for identifying the
如图4所示,极性检测组件8包括固定架9、驱动器10、安装架11和探针工装板15,驱动器10驱动安装架11相对固定架9升降运动,探针工装板15可拆卸连接在安装架11上。锂电池电芯组28极性快速检测装置包括机架1,极性检测组件8位于倍速链2的一侧。在一些实施例中,固定架9固定连接在机架1上,安装架11固定连接驱动器10的伸缩端,驱动器10可以是直线电机。固定架9上具有沿高度方向设置的导轨,安装架11通过导轨的导向相对固定架9上下升降并带动以可拆卸连接的方式连接在安装架11上的探针工装板15进行升降。探针工装板15的竖向投影位于倍速链2上。通过上述结构,实现探针工装板15上的探针与到位的电芯组28上的极柱接触。As shown in Figure 4, the
如图5和7所示,安装架11包括工装滑槽12,探针工装板15插入到工装滑槽12中,探针工装板15可拆卸连接工装滑槽12,采用插入形式操作简单,便于快速更换探针工装板15。沿着探针工装板15板面的垂向方向,工装滑槽12安装有用于手拧的蝶形螺丝,操作者可以做到免工具拧转蝶形螺丝,使蝶形螺丝在工装滑槽12上沿探针工装板15板面的垂向方向进给从而抵接在探针工装板15上,限制其上下位置。探针工装板15上具有若干探针单元16,探针单元16设有对应电芯的正负极柱的探针。探针单元16除了探针以外还具有探针板,探针板的两端分别具有长圆孔,探针板经紧固件固定连接在探针工装板15。根据电芯组28中的相邻极柱在长度和宽度方向的排列间距,探针单元16进行对应阵列排布。一探针单元16上固定连接有两探针,两探针之间的距离与需要检测的电芯组28中的电芯上的极柱之间的距离相同。在一些实施例中,沿着探针单元16的长度方向,探针单元16的两端分别具有两根探针,共计四根探针,这四根探针的连线为直线,该结构可以适应不同极柱间距的电芯,提高探针单元16的复用率,提高探针单元16对不同极柱间距的电芯的兼容性。在一些实施例中,探针靠近电芯的一端具有若干锯齿,该结构进一步提升了可靠性。与电芯在电芯组28中的排列相同,探针单元16也在探针工装板15上对应排列。通过上述特征,使得各个探针与各个极柱之间均可以做到同时接触,避免由于虚接造成的检测错误。工装滑槽12设有用于指示定位探针工装板15到位的侧边挡块13,侧边挡块13可调节连接在工装滑槽12上。根据不同极柱间距的电芯组28,可以更换对应的探针工装板15,调整侧边挡块13的位置以使得探针与极柱对齐。在一些实施例中,沿着探针工装板15的长度方向,侧边挡块13至少有一部分位于探针工装板15的投影,侧边挡块13的两端连接有呈“L”字形的标记卡14,标记卡14位于工装滑槽12的外缘,紧固件通过标记卡14和侧边挡块13连接工装滑槽12,在工装滑槽12上划刻标记线指示标记卡14;或者,在标记卡14设置延伸板,通过将延伸板与工装滑槽12的端部对齐以调节工装滑槽12的位置,从而快速定位。As shown in Figures 5 and 7, the mounting
如图3所示,修复台17和顶升平移机构21配合在倍速链2和修复台17之间移动电芯组28。倍速链2包括上层倍速链5和下层倍速链6以及装载在上层倍速链5或下层倍速链6上的回流工装板7,所述电芯组28置于上层倍速链5的回流工装板7上。上层倍速链5和下层倍速链6的输送方向相反,上层倍速链5将电芯组28和回流工装板7向下游工序位置输送,下层倍速链6将从下游倍速链2返回的回流工装板7反向送回锂电池电芯组28极性快速检测装置的上游,省去人工搬回回流工装板7的人工。将送料倍速链2和回流倍速链2上下设置,节约了空间。顶升平移机构21包括上层顶升平移机构26和下层顶升平移机构27,上层平移机构移动上层倍速链5的回流工装板7,下层顶升平移机构27移动下层倍速链6的回流工装板7。顶升平移机构21包括升降结构和平移结构,升降结构将回流工装板7顶出倍速链2的导槽,平移结构将回流工装板7平移。修复台17配合进行接收,将回流工装板7移动至修复台17。若电芯组28无法进行修复,在移除电芯组28后,将空置的回流工装板7平移至下层顶升平移机构27,然后下层顶升平移机构27复位,由下层倍速链6将空置的回流工装板7送回。As shown in FIG. 3 , the repair station 17 and the jacking and
如图9和10所示,具体的,顶升平移装置包括升降电机22、升降台23、平移电机24和位于升降台23长度方向两端且沿宽度方向设置的平移链25,升降电机22将升降台23顶起,使得升降台23上的回流工装板7的底面超出倍速链型材4的顶部,平移电机24驱动升降台23上的平移链25转动,带动回流工装板7向修复台17方向运动。As shown in Figures 9 and 10, specifically, the lifting translation device includes a lifting
如图8所示,修复台17包括剃废升降机18和连接在剃废升降机18上的剃废架19,剃废架19上设有平移电机24和沿倍速链2宽度方向设置的平移链25。剃废升降机18作为修复台17的一部分,起到对接顶升平移机构21和提供操作平台的作用。在一些实施例中,修复台17还包括用于展示错误排列的电芯的位置的屏幕20,用于控制剃废架19和顶升平移装置运动的控制按钮以及在极性检测组件8识别错误时主动放行的相关按钮。As shown in Figure 8, the repair station 17 includes a shaving
在本申请中,整个流程包括:倍速链2将电芯组28输送到极性检测组件8的检测位置;极性检测组件8上的探针与电芯组28的极柱进行接触,然后进行检测,获取电芯组28的状态并传回控制器中,控制器获取电芯组28的状态根据预设条件将其通过倍速链2向下一流程输送或通过顶升平移机构21配合修复台17将电芯组28输送至修复台17进行修复,待修复完成后再将电芯组28输送回。本装置对电芯组28中的电芯逐一测量,判断其顺序,无需人工肉眼判断,精度更高,物料的报废几率更小,也更为节省人工。In this application, the whole process includes: the double-
如图6所示,在一些实施例中,探针单元16弹性安装在探针工装板15上,当极性检测组件8的驱动器10由于精度或调节或安装的问题造成探针工装板15下降过多时,探针工装板15上的探针会与电芯组28的极柱发生撞针,所述结构可以为探针提供一定的活动余量,从而保护探针。具体的,探针单元16的两端设有导向柱29,导向柱29固接有紧固件。导向柱29插装在探针工装板15上,探针单元16的板面与探针工装板15之间设有弹簧30,其中,至少有一弹簧30的两端伸出有接触簧片31,板材上设有磁环33,磁环33位于弹簧30内,弹簧30在自然状态下,接触簧片31分离,在压缩状态下,接触簧片31贴合并使得弹簧30形成闭合回路,一接触簧片31串联有电流传感器32,电流传感器32连接控制器,控制器根据电流传感器32的信号控制驱动器10,具体的,磁环33和弹簧30表面作绝缘处理。当探针接触极柱并造成弹簧30压缩时,弹簧30形成闭合回路,磁环33随着导向杆继续运动,根据电磁感应效应,在闭合回路中产生电流,电流传感器32捕获到电流信号,输送给控制器,根据电流传感器32控制驱动器10停机,探针工装板15不再下移,该结构起到了对探针工装板15的保护作用,避免探针单元16或电芯组28撞伤。As shown in Figure 6, in some embodiments, the
本装置是这样工作的:首先,倍速链2工作,沿流程方向输送电芯组28,当到位传感器检测到电芯组28后,挡位工装工作,挡位块顶住承载电芯组28的回流工装板7;扫码器扫描电芯组28的识别码,将电芯组28的信号输送给控制器,控制器根据电芯组28的型号屏蔽极性检测组件8的多余探针,并控制极性检测组件8中的安装架11下降使得探针与电芯组28的极柱接触并进行测量。测量得到的结果返回至控制器根据其预设参数判断电芯组28的状态。若电芯组28的状态符合要求则挡位工装工作,挡位块降下,倍速链2工作带动电芯组28继续向下一流程输送;若电芯组28的状态不符合要求则上层顶升平移装置工作,将对应的回流工装板7顶升超出倍速链型材4高度,然后上层顶升平移装置的平移电机24工作驱动平移链25带动对应的回流工装板7横向移动,此时修复台17的剃废升降机18工作将剃废架19移动至与上层顶升平移装置的升降台23平齐位置,剃废架19上的平移链25也同步转动,将对应的回流工装板7输送至剃废架19上,然后剃废架19上升至方便人操作的位置。电芯组28的状态输送至修复台17并以屏幕20的形式展示出来,工作人员进行修复,若已完成修复,则将通过控制按钮控制剃废升降机18、剃废架19以及对应的顶升平移装置再次对接,将回流工装板7转移回上层倍速链本体3上,再次对其进行检测;若确认电芯组28无法修复,则通过人工或机械臂的形式将电芯组28移除后,通过剃废升降机18、剃废架19与下层顶升平移机构27对接,将空载的回流工装板7移动至下层倍速链6上。The device works like this: First, the double-
以上所述的实施例只是本发明的较佳的方案,并非对本发明作任何形式上的限制,在不超出权利要求所记载的技术方案的前提下还有其它的变体及改型。The embodiments described above are only preferred solutions of the present invention, and do not limit the present invention in any form. There are other variations and modifications on the premise of not exceeding the technical solutions described in the claims.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210793828.1A CN115295855B (en) | 2022-07-07 | 2022-07-07 | A battery cell polarity detection and repair integrated device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210793828.1A CN115295855B (en) | 2022-07-07 | 2022-07-07 | A battery cell polarity detection and repair integrated device |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115295855A true CN115295855A (en) | 2022-11-04 |
| CN115295855B CN115295855B (en) | 2026-03-20 |
Family
ID=83822834
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210793828.1A Active CN115295855B (en) | 2022-07-07 | 2022-07-07 | A battery cell polarity detection and repair integrated device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115295855B (en) |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN206327871U (en) * | 2016-12-07 | 2017-07-14 | 东莞市天蓝智能装备有限公司 | Lithium battery double-speed chain jacking and translation device |
| CN207752125U (en) * | 2018-01-12 | 2018-08-21 | 深圳市欧盛自动化有限公司 | Power battery detection machine |
| CN208413150U (en) * | 2018-06-13 | 2019-01-22 | 浙江大华科技有限公司 | A kind of jacking translation mechanism and production line |
| CN109283467A (en) * | 2018-10-22 | 2019-01-29 | 盐城国投中科新能源科技有限公司 | A battery polarity detection device |
| CN214242473U (en) * | 2020-12-09 | 2021-09-21 | 贵州聚能世纪科技有限责任公司 | Novel energy storage vanadium cell pile production is carried device |
| CN218470946U (en) * | 2022-07-07 | 2023-02-10 | 浙江南都电源动力股份有限公司 | Quick detection device of lithium cell electric core group polarity |
-
2022
- 2022-07-07 CN CN202210793828.1A patent/CN115295855B/en active Active
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN206327871U (en) * | 2016-12-07 | 2017-07-14 | 东莞市天蓝智能装备有限公司 | Lithium battery double-speed chain jacking and translation device |
| CN207752125U (en) * | 2018-01-12 | 2018-08-21 | 深圳市欧盛自动化有限公司 | Power battery detection machine |
| CN208413150U (en) * | 2018-06-13 | 2019-01-22 | 浙江大华科技有限公司 | A kind of jacking translation mechanism and production line |
| CN109283467A (en) * | 2018-10-22 | 2019-01-29 | 盐城国投中科新能源科技有限公司 | A battery polarity detection device |
| CN214242473U (en) * | 2020-12-09 | 2021-09-21 | 贵州聚能世纪科技有限责任公司 | Novel energy storage vanadium cell pile production is carried device |
| CN218470946U (en) * | 2022-07-07 | 2023-02-10 | 浙江南都电源动力股份有限公司 | Quick detection device of lithium cell electric core group polarity |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115295855B (en) | 2026-03-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103529383B (en) | Automatic testing equipment | |
| CN109378153B (en) | A fully automatic multi-pole magnetization and detection integrated equipment | |
| CN110031711B (en) | Small motor carbon brush holder detection system and test method | |
| CN208223398U (en) | A kind of product detection device based on machine vision | |
| CN109158338B (en) | Vertical material sorting all-in-one of getting of lithium cell | |
| CN212349526U (en) | Battery core surface defect detection device | |
| CN112903699B (en) | Automatic microscopic examination equipment for busbar | |
| CN205484707U (en) | Alternating current contactor automation test equipment | |
| CN110817241B (en) | Detection apparatus for PCB board | |
| CN111268230A (en) | Multi-tube type blood collection tube labeling machine and labeling method | |
| CN108987842A (en) | A kind of Battery recycling disassembling method | |
| CN218470946U (en) | Quick detection device of lithium cell electric core group polarity | |
| CN107607866A (en) | A switch test method based on switch test equipment | |
| CN110420891A (en) | Battery core detects sorting unit and method | |
| CN203196912U (en) | Automatic shifting control device of power lithium battery | |
| CN211733041U (en) | A fully automatic battery sorting equipment | |
| CN112657851A (en) | Appearance detection device and method | |
| CN109596193B (en) | Automatic test equipment for meter | |
| CN111256639A (en) | Piston Ring Inspection Line | |
| CN110665858A (en) | Electricity core OCV test machine | |
| CN114740015A (en) | Revolution and rotation detection device and method | |
| CN212747554U (en) | Go-no go gauge automatic detection machine for detecting threaded hole | |
| CN115295855B (en) | A battery cell polarity detection and repair integrated device | |
| CN109324283A (en) | An automatic conveying circuit board equipment for X-ray testing | |
| CN211696885U (en) | Rotation type multistation liquid crystal module detection device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |