CN114789210A - Clamping and fixing method for drawing and bending process of thin-walled open profiles - Google Patents
Clamping and fixing method for drawing and bending process of thin-walled open profiles Download PDFInfo
- Publication number
- CN114789210A CN114789210A CN202210478442.1A CN202210478442A CN114789210A CN 114789210 A CN114789210 A CN 114789210A CN 202210478442 A CN202210478442 A CN 202210478442A CN 114789210 A CN114789210 A CN 114789210A
- Authority
- CN
- China
- Prior art keywords
- thin
- walled
- lining
- profile
- clamping
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D7/00—Bending rods, profiles, or tubes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D43/00—Feeding, positioning or storing devices combined with, or arranged in, or specially adapted for use in connection with, apparatus for working or processing sheet metal, metal tubes or metal profiles; Associations therewith of cutting devices
- B21D43/003—Positioning devices
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Clamps And Clips (AREA)
- Automatic Assembly (AREA)
Abstract
Description
技术领域technical field
本发明涉及工装夹具技术领域,特别是一种薄壁开口型材拉弯工序装夹固定方法。The invention relates to the technical field of tooling and fixtures, in particular to a clamping and fixing method in the drawing and bending process of thin-walled open profiles.
背景技术Background technique
汽车的前后碰撞横梁是一种常见的开口型材,其在加工过程中需经历拉弯操作整体弯曲成一定的弧度,其经过拉弯操作后的状态如图10所示。一方面,前后碰撞横梁通常为铝合金材质,其具有较好的可塑性以满足拉弯过程中的形变需求,另一方面,为了适应汽车轻量化的要求,前后碰撞横梁的厚度设计的相对较薄,并通过设置加强筋或凸台结构提升强度。The front and rear collision beam of an automobile is a common open profile, which needs to undergo a stretch-bending operation to be bent into a certain radian as a whole during the processing process. The state after the stretch-bending operation is shown in Figure 10. On the one hand, the front and rear collision beams are usually made of aluminum alloy, which has good plasticity to meet the deformation requirements during the stretching and bending process. On the other hand, in order to meet the requirements of lightweight automobiles, the thickness of the front and rear collision beams is relatively thin. , and improve the strength by setting stiffeners or boss structures.
基于上述的两个因素,前后碰撞横梁在拉弯中存在以下问题:1、拉弯工序所用夹具的装夹位置通常位于型材的两端,由于型材壁厚较薄,夹紧力过大则很容易将型材夹塌陷,夹紧力过小则容易在拉弯过程中夹具出现夹头滑移甚至松脱;2、拉弯过程中,型材在靠近弧形内侧的区域会产生材料挤压堆积的趋势,型材在靠近弧形外侧的区域会产生材料拉伸延展的趋势,这会导致型材在拉弯后出现截面畸变,边缘起皱的现象,严重影响成形质量;并且,随着弯曲程度的增大,截面畸变和边缘起皱现象愈发严重,这严重限制了型材的可弯曲程度;3、若型材中部存在隐裂纹等材料缺陷,在拉弯过程中,材料缺陷处会产生应力集中,存在型材突然断裂,向外弹开的隐患。Based on the above two factors, the front and rear collision beams have the following problems in the drawing and bending: 1. The clamping positions of the clamps used in the drawing and bending process are usually located at both ends of the profile. Due to the thin wall thickness of the profile, the clamping force is too large. It is easy to collapse the profile clamp, and if the clamping force is too small, the clamp will easily slip or even loosen during the bending process; 2. During the bending process, the material will be squeezed and accumulated in the area near the inner side of the arc. In the area near the outer side of the arc, the profile will have a tendency to stretch and extend the material, which will lead to the section distortion and wrinkling of the edge after the profile is stretched and bent, which seriously affects the forming quality; and, with the increase of the bending degree. Large, the cross-section distortion and edge wrinkling become more and more serious, which seriously limits the bendability of the profile; 3. If there are material defects such as hidden cracks in the middle of the profile, during the bending process, stress concentration will occur at the material defects, and there are There is a danger that the profile suddenly breaks and bounces outwards.
发明内容SUMMARY OF THE INVENTION
本发明的目的是克服现有技术的不足,而提供一种薄壁开口型材拉弯工序装夹固定方法,它用于薄壁开口型材拉弯工序的装夹固定,解决了薄壁开口型材在拉弯时存在夹持不便,变形起皱,断裂外弹风险的问题。The purpose of the present invention is to overcome the deficiencies of the prior art, and to provide a clamping and fixing method for the drawing and bending process of thin-walled open profiles, which is used for the clamping and fixing of the drawing and bending process of thin-walled open profiles, and solves the problem of There are problems of inconvenient clamping, deformation and wrinkling, and the risk of breakage and bounce during bending.
本发明的技术方案是:一种薄壁开口型材拉弯工序装夹固定方法,基于薄壁开口型材拉弯工序工装总成,可对薄壁开口型材执行拉弯工序提供良好的装夹固定支持;所述的薄壁开口型材上设有U形槽,U形槽一端封闭,另一端开口,开口处的两边沿向开口外侧翻展而形成翻边;The technical scheme of the present invention is: a clamping and fixing method for the drawing and bending process of thin-walled open profiles. Based on the tooling assembly for the drawing and bending process of thin-walled open profiles, it can provide good clamping and fixing support for performing the drawing and bending process of thin-walled open profiles. The thin-walled opening profile is provided with a U-shaped groove, one end of the U-shaped groove is closed, the other end is open, and the two edges of the opening are turned to the outside of the opening to form a flanging;
薄壁开口型材拉弯工序工装总成,包括夹头装置、柔性衬包组件和侧壁夹持组件;A thin-walled open profile drawing and bending process tooling assembly, including a collet device, a flexible lining package assembly and a side wall clamping assembly;
两组夹头装置分别用于夹持薄壁开口型材的两端;夹头装置包括外壳、弹簧螺栓、连接座、压块A、压块B、动力轴和端部内衬块;Two sets of collet devices are respectively used to clamp both ends of thin-walled open profiles; the collet device includes shell, spring bolt, connecting seat, pressure block A, pressure block B, power shaft and end lining block;
外壳呈套筒形,其内孔壁面为锥面,其两端分别设有连通至外壳内孔的型材装取口和动力接入口,其外圆面上环形均布有四个连通至外壳内孔的腰形孔,腰形孔的延伸方向平行于外壳轴向方向;The casing is sleeve-shaped, and its inner hole wall is a conical surface. The two ends of the casing are respectively provided with a profile loading and unloading port and a power inlet that communicate with the inner hole of the casing. The waist-shaped hole of the hole, the extension direction of the waist-shaped hole is parallel to the axial direction of the shell;
连接座一侧设有用于贴合外壳内孔壁面的凸弧面,连接座另一侧设有安装面和插接部A;四个连接座呈环形均布在外壳内孔中,并呈两两相对布置;One side of the connection seat is provided with a convex arc surface for fitting the wall surface of the inner hole of the casing, and the other side of the connection seat is provided with a mounting surface and a plug-in part A; the four connection seats are uniformly distributed in the inner hole of the outer casing in two shapes. two opposite arrangements;
弹簧螺栓头部一端位于外壳外部,弹簧螺栓杆部一端穿过外壳上的腰形孔,而伸入外壳内孔中,并与连接座螺纹连接;弹簧螺栓通过弹力迫使连接座的凸弧面压紧在外壳内孔壁面上;One end of the head of the spring bolt is located outside the casing, and one end of the stem of the spring bolt passes through the waist-shaped hole on the casing, extends into the inner hole of the casing, and is threadedly connected with the connecting seat; the spring bolt forces the convex arc surface of the connecting seat to press through the elastic force. tightly on the wall of the inner hole of the shell;
两个压块A可拆卸连接在其中两个相对布置的连接座的安装面上,并相对布置;两个压块B可拆卸连接在另外两个相对布置的连接座的安装面上,并相对布置;两个压块A与两个压块B合围形成容纳区间,容纳区间与外壳的型材装取口直接连通;The two pressing blocks A are detachably connected to the mounting surfaces of the two oppositely arranged connecting seats, and are arranged oppositely; the two pressing blocks B are detachably connected to the mounting surfaces of the other two oppositely arranged connecting seats, and are opposite to each other. Arrangement; two pressing blocks A and two pressing blocks B are enclosed to form a accommodating area, and the accommodating area is directly connected with the profile loading and unloading port of the shell;
动力轴活动安装在外壳的动力接入口上,其前端伸出在外壳外部,以接收外部动力,其后端伸入外壳内腔,其后端设有插接部B;动力轴通过插接部B与四个连接座的插接部A活动插接;动力轴在外部动力的驱动下沿外壳轴向方向做往复直线运动,进而通过插接部B与插接部A的插接结构带动四个连接座沿外壳内孔壁面同步移动,以扩大或缩小容纳区间;The power shaft is movably installed on the power inlet of the casing, its front end protrudes outside the casing to receive external power, its rear end extends into the inner cavity of the casing, and its rear end is provided with a plug-in part B; the power shaft passes through the plug-in part B is movably plugged with the plug parts A of the four connection bases; the power shaft reciprocates linearly along the axial direction of the casing under the drive of external power, and then drives the four plug parts through the plug structure of the plug parts B and A Each connecting seat moves synchronously along the inner hole wall of the shell to expand or shrink the accommodation area;
端部内衬块上设有两个相对的侧立面和设在两个侧立面之间的上、下端面,端部内衬块上还设有两条贯通上、下端面的插槽,端部内衬块的下端面两侧分别设有缺口;端部内衬块活动安装在容纳区间内,其两个侧立面被夹紧在两个压块A之间,其上端面与压块B之间形成间隙;两条插槽在上端分别连通至间隙的两侧,两条插槽在下端各与一个缺口连通,从而使间隙、插槽、缺口依次连通而形成与薄壁开口型材形状相适应的夹持区间;The end lining block is provided with two opposite side elevations and upper and lower end faces arranged between the two side elevations, and the end lining block is also provided with two slots penetrating the upper and lower end faces , there are gaps on both sides of the lower end face of the end lining block; the end lining block is movably installed in the accommodating area, and its two side elevations are clamped between the two pressing blocks A, and its upper end face and A gap is formed between the pressing blocks B; the two slots are connected to both sides of the gap at the upper end, respectively, and the two slots are connected to a gap at the lower end, so that the gap, the slot, and the gap are connected in turn to form a thin-walled opening. The clamping interval suitable for the shape of the profile;
柔性衬包组件安装在薄壁开口型材上,并位于薄壁开口型材在两个夹头装置之间的长度段上;柔性衬包组件包括中部柔性内衬和中部包口外衬;The flexible lining package assembly is installed on the thin-walled opening profile, and is located on the length of the thin-walled opening profile between the two chuck devices; the flexible lining package assembly includes a middle flexible inner lining and a middle opening outer lining;
中部柔性内衬为条形构件,其活动安装在薄壁开口型材的U形槽中,并与薄壁开口型材的U形槽的形状相适应;定义中部柔性内衬与U形槽底部正对的一侧表面为面A,定义中部柔性内衬朝向U形槽开口的一侧表面为面B,定义中部柔性内衬正对U形槽两侧壁的表面为面C;中部柔性内衬上沿长度方向间隔设有多条辅助变形槽A,辅助变形槽A从面B向面A延伸,并将两个面C贯通;The middle flexible lining is a strip-shaped member, which is movably installed in the U-shaped groove of the thin-walled opening profile, and is adapted to the shape of the U-shaped groove of the thin-walled opening profile; it is defined that the middle flexible lining is opposite to the bottom of the U-shaped groove. The side surface of the middle flexible lining is defined as face A, the side surface of the middle flexible lining facing the opening of the U-shaped groove is defined as face B, and the surface of the middle flexible lining facing the two side walls of the U-shaped groove is defined as face C; A plurality of auxiliary deformation grooves A are arranged at intervals along the length direction, and the auxiliary deformation grooves A extend from the surface B to the surface A, and pass through the two surfaces C;
中部包口外衬为条形构件,其一侧表面上设有沿长度方向延伸且槽深由深至浅依次布置的内侧槽和外侧槽,外侧槽设在内侧槽的外部并将内侧槽包容在内;中部包口外衬一方面通过内侧槽与中部柔性内衬活动插接,另一方面通过外侧槽将薄壁开口型材开口及两翻边包容在内;定义中部包口外衬设有内侧槽和外侧槽的一侧表面为面D,定义中部包口外衬与面D相对的一侧表面为面E,定义中部包口外衬设在面D与面E之间并平行于中部包口外衬长度方向的两个侧立面为面F;中部包口外衬上沿长度方向间隔设有多条辅助变形槽B,辅助变形槽B从面D向面E延伸,并将两个面F贯通;The outer lining of the middle bag mouth is a strip-shaped member, and its one side surface is provided with an inner groove and an outer groove extending along the length direction and the groove depth is arranged in sequence from deep to shallow, and the outer groove is provided outside the inner groove and contains the inner groove. Inside; the outer lining of the middle bag mouth is movably plugged with the middle flexible inner lining through the inner groove on the one hand, and the opening of the thin-walled open profile and the two flanges are contained by the outer groove on the other hand; the outer lining of the middle bag mouth is defined with inner grooves and The surface of one side of the outer groove is surface D, and the surface of the side opposite to the surface D is defined as the surface E, and the outer lining of the middle opening is defined as being arranged between the surface D and the surface E and parallel to the length direction of the outer lining of the middle opening The two side elevations of the side are face F; the outer lining of the middle bag mouth is provided with a plurality of auxiliary deformation grooves B at intervals along the length direction, and the auxiliary deformation grooves B extend from the face D to the face E, and pass through the two faces F;
多组侧壁夹持组件沿薄壁开口型材的长度方向间隔安装在薄壁开口型材上,并位于薄壁开口型材在两个夹头装置之间的长度段上;侧壁夹持组件包括大力钳和分别焊接在大力钳两个钳嘴处的垫块;大力钳通过两个垫块活动装夹在薄壁开口型材的两面相对的外侧壁面上;A plurality of groups of side wall clamping components are installed on the thin-walled opening profiles at intervals along the length direction of the thin-walled opening profiles, and are located on the length of the thin-walled opening profiles between the two clamping devices; the side wall clamping components include a large force pliers and spacers welded at the two jaws of the pliers respectively; the pliers are movably clamped on the opposite outer side walls of the thin-walled opening profile through the two spacers;
装夹固定方法如下:The clamping method is as follows:
S01,对薄壁开口型材进行充填及包口:S01, filling and wrapping thin-walled opening profiles:
1、将中部柔性内衬安装在薄壁开口型材的U形槽中,安装到位后,中部柔性内衬位于U形槽的中部区段,中部柔性内衬的面A与U形槽底部正对并贴合,中部柔性内衬的两个面C分别与U形槽两侧壁正对并贴合;1. Install the middle flexible lining in the U-shaped groove of the thin-walled open profile. After the installation is in place, the middle flexible lining is located in the middle section of the U-shaped groove, and the surface A of the middle flexible lining is opposite to the bottom of the U-shaped groove. And fit, the two surfaces C of the middle flexible lining are facing and fit with the two side walls of the U-shaped groove respectively;
2、将中部包口外衬安装在薄壁开口型材的U形槽开口处,并确保其与中部柔性内衬的位置相对,一方面其通过内侧槽与中部柔性内衬活动插接,另一方面其通过外侧槽将薄壁开口型材的开口及两翻边包容在内,再一方面其通过外侧槽与内侧槽之间的台阶面与薄壁开口型材的两翻边贴合;2. Install the outer lining of the middle bag opening at the opening of the U-shaped groove of the thin-walled opening profile, and ensure that it is opposite to the position of the middle flexible lining. On the one hand, it is movably inserted into the middle flexible lining through the inner groove, and on the other hand The opening of the thin-walled open profile and the two flanges are contained by the outer groove, and on the other hand, it is attached to the two flanges of the thin-walled open profile through the stepped surface between the outer groove and the inner groove;
3、将两个端部内衬块分别安装在薄壁开口型材的两端,从而对薄壁开口型材的U形槽两端进行填充,安装到位后,薄壁开口型材的U型槽两侧壁分别穿过端部内衬块的两条插槽,端部内衬块通过两条插槽之间的区域将U形槽填充;3. Install the two end lining blocks on both ends of the thin-walled open profile, so as to fill both ends of the U-shaped groove of the thin-walled open profile. After the installation is in place, the two sides of the U-shaped groove of the thin-walled open profile The wall passes through the two slots of the end lining block respectively, and the end lining block fills the U-shaped groove through the area between the two slots;
本步骤完成时,薄壁开口型材的U形槽的全长被中部柔性内衬和两个端部内衬块填充满;When this step is completed, the full length of the U-shaped groove of the thin-walled open profile is filled with the middle flexible lining and the two end lining blocks;
S02,将夹头装置调节至初始状态:S02, adjust the chuck device to the initial state:
1、将两组夹头装置的动力轴前端分别与拉弯机的动力输出部件连接,并控制拉弯机的动力输出部件动作,使两组夹头装置相互正对布置,并处在相距最远的距离;1. Connect the front ends of the power shafts of the two sets of collet devices to the power output parts of the stretch bender respectively, and control the action of the power output parts of the stretch bender, so that the two sets of collet devices are arranged in front of each other and at the most distance from each other. far distance;
2、驱动动力轴沿外壳轴向方向移动,进而通过动力轴的插接部B与四个连接座的插接部A的配合关系,带动四个连接座沿外壳内孔壁面同步移动,将容纳区间扩大至极限;2. Drive the power shaft to move in the axial direction of the casing, and then drive the four connecting bases to move synchronously along the inner hole wall of the casing through the mating relationship between the plug-in part B of the power shaft and the plug-in parts A of the four connection bases, which will accommodate The interval is expanded to the limit;
本步骤中,拉弯机的动力输出部件一方面用于驱动动力轴做水平直线移动,另一方面用于驱动夹头装置做水平弧形轨迹摆动和/或水平直线移动和/或竖向直线移动;In this step, on the one hand, the power output part of the stretch bender is used to drive the power shaft to move horizontally and linearly, and on the other hand, it is used to drive the chuck device to perform horizontal arc trajectory swing and/or horizontal straight movement and/or vertical straight line move;
S03,装夹固定薄壁开口型材:S03, clamping and fixing thin-walled opening profiles:
1、将进行了充填和包口的薄壁开口型材吊至水平,并使其两端分别正对两个夹头装置的型材装取口;1. Lift the thin-walled open profile that has been filled and wrapped to the level, and make its two ends face the profile loading and unloading ports of the two chuck devices respectively;
2、控制拉弯机的动力输出部件动作,使两组夹头装置做相向水平直线移动,从而使薄壁开口型材的两端分别通过两个夹头装置的型材装取口伸入两个夹头装置的容纳区间中;2. Control the action of the power output part of the stretch-bender, so that the two sets of collet devices move horizontally and straightly, so that the two ends of the thin-walled open profiles extend into the two clips through the profile loading and unloading ports of the two collet devices respectively. in the accommodating area of the head device;
3、控制拉弯机的动力输出部件动作,驱动动力轴沿外壳轴向方向移动,进而通过动力轴的插接部B与四个连接座的插接部A的配合关系,带动四个连接座沿外壳内孔壁面同步移动,将容纳区间缩小,直至夹紧薄壁开口型材的端部;3. Control the action of the power output component of the stretch bender, drive the power shaft to move in the axial direction of the casing, and then drive the four connecting seats through the matching relationship between the plug-in part B of the power shaft and the plug-in parts A of the four connecting seats Move synchronously along the wall of the inner hole of the shell to reduce the accommodating area until the end of the thin-walled opening profile is clamped;
4、将多组侧壁夹持组件沿薄壁开口型材的长度方向间隔安装在薄壁开口型材上,具体是将大力钳调整为夹紧状态,从而使连接在大力钳两个钳嘴上的垫块压紧在薄壁开口型材的两面相对的外侧壁面上;4. Install multiple sets of side wall clamping components on the thin-walled open profile at intervals along the length direction of the thin-walled open profile, specifically, adjust the forceps to the clamping state, so that the clamps connected to the two jaws of the forceps The spacer is pressed against the two opposite outer side walls of the thin-walled opening profile;
本步骤完成时,薄壁开口型材被两个夹头装置共同夹持,两个压块A分别压紧端部内衬块的两个侧立面,位于上端的压块B通过其下表面压紧薄壁开口型材的封闭端外壁面,位于下端的压块B通过其上表面压紧薄壁开口型材的两翻边及端部内衬块的下端面。When this step is completed, the thin-walled open profile is jointly clamped by the two clamping devices, the two pressing blocks A press the two side elevations of the end lining block respectively, and the pressing block B at the upper end is pressed by its lower surface Tighten the outer wall surface of the closed end of the thin-walled open profile, and the pressing block B at the lower end presses the two flanges of the thin-walled open profile and the lower end surface of the end lining block through its upper surface.
本发明进一步的技术方案是:S03步骤中,两组相邻的侧壁夹持组件之间的间距应在满足下述条件的前提下取最小值;所述条件为:在薄壁开口型材拉弯过程中,两组相邻的侧壁夹持组件不产生干涉。A further technical solution of the present invention is: in step S03, the distance between two groups of adjacent side wall clamping components should be the minimum value under the premise of satisfying the following conditions; During the bending process, the two adjacent side wall clamping assemblies do not interfere.
本发明进一步的技术方案是:两个压块A分别在相对布置的表面上设有纵横交错的防滑纹路;两个压块B分别在相对布置的表面上设有纵横交错的防滑纹路。A further technical solution of the present invention is that: the two pressing blocks A are respectively provided with crisscross anti-skid lines on the oppositely arranged surfaces;
本发明再进一步的技术方案是:端部内衬块的缺口深度与薄壁开口型材的翻边厚度相适应;当薄壁开口型材装夹在夹持区间内时,端部内衬块的下端面与薄壁开口型材的两个翻边齐平。A further technical solution of the present invention is: the notch depth of the end lining block is adapted to the flanging thickness of the thin-walled open section; when the thin-walled open section is clamped in the clamping area, the lower part of the end lining The end faces are flush with the two flanges of the thin-walled open profile.
本发明更进一步的技术方案是:插接部A为设在连接座上的定位孔,插接部B为设在动力轴后端的圆柱凸台,所述圆柱凸台的形状与所述定位孔的形状相适应,从而实现插接部A与插接部B的活动插接。A further technical solution of the present invention is: the plug-in part A is a positioning hole arranged on the connecting seat, and the plug-in part B is a cylindrical boss set at the rear end of the power shaft, and the shape of the cylindrical boss is the same as that of the positioning hole. The shape of the socket is adapted to the shape of the socket, so as to realize the movable plug connection of the plug-in part A and the plug-in part B.
本发明与现有技术相比具有如下优点:Compared with the prior art, the present invention has the following advantages:
1、其用于薄壁开口型材拉弯工序的装夹固定。一方面通过柔性衬包组件和侧壁夹持组件的配合,对薄壁开口型材的U形槽进行充填、开口及翻边进行包口、外侧壁面进行压实,实现了立体全方位的保护,有效避免了薄壁开口型材在拉弯过程中出现变形、起皱、断裂等问题。另一方面通过夹头装置中的端部内衬块对薄壁开口型材的内壁进行了有效衬托,有效避免了薄壁开口型材在夹紧力的作用下被夹塌陷或溃缩,使薄壁开口型材能耐受相对更大的夹紧力,装夹牢固性得到了保障。1. It is used for clamping and fixing in the drawing and bending process of thin-walled open profiles. On the one hand, through the cooperation of the flexible lining package component and the side wall clamping component, the U-shaped groove of the thin-walled opening profile is filled, the opening and flanging are packaged, and the outer side wall surface is compacted, so as to realize the three-dimensional and all-round protection. It effectively avoids the problems of deformation, wrinkling and breakage of thin-walled open profiles during the stretching and bending process. On the other hand, the inner wall of the thin-walled open profile is effectively foiled by the end lining block in the chuck device, which effectively prevents the thin-walled open profile from being clamped or collapsed under the action of the clamping force, making the thin-walled open profile The open profile can withstand relatively larger clamping forces, and the clamping firmness is guaranteed.
2、夹头装置装夹或卸下型材的过程简单易操作,仅需驱动动力轴沿外壳轴向方向做往复直线运动,即可实现四个连接座的同步移动,进而实现型材的夹紧或放松。2. The process of clamping or unloading the profile by the chuck device is simple and easy to operate. It only needs to drive the power shaft to make a reciprocating linear motion along the axial direction of the housing to realize the synchronous movement of the four connecting seats, thereby realizing the clamping or the profile of the profile. Relax.
3、夹头装置可通过更换压块A、压块B及端部内衬块,使其适应于不同截面形状的型材,故其具有良好的通用性(泛用性)。3. The chuck device can adapt to the profiles of different cross-sectional shapes by replacing the pressing block A, the pressing block B and the end lining block, so it has good versatility (universality).
4、夹头装置中的端部内侧块通过插槽和缺口的设计,可使型材与端部内衬块连接后型材形成一个多壁面均无台阶的方正整体,一方面便于压块A和压块B施压夹紧,另一方面也降低了压块A和压块B的结构设计难度。4. The end inner block in the collet device is designed with slots and gaps, so that the profile can be connected to the end lining block to form a square whole with multiple walls and no steps. On the one hand, it is convenient for pressing block A and pressing The block B is pressed and clamped, and on the other hand, the structural design difficulty of the pressure block A and the pressure block B is also reduced.
5、柔性衬包组件中的中部柔性内衬上间隔设有多条辅助变形槽A,柔性衬包组件中的中部包口外衬上间隔设有多条辅助变形槽B,基于该设计,当型材弯曲时,柔性衬包组件能够很好的贴合型材同步弯曲,对型材的衬托效果较好,不易发生断裂及弯曲过量难以复原的情况。5. A plurality of auxiliary deformation grooves A are arranged at intervals on the middle flexible inner lining of the flexible lining bag assembly, and a plurality of auxiliary deformation grooves B are arranged at intervals on the outer lining of the middle bag mouth in the flexible lining bag assembly. Based on this design, when the profile is When bending, the flexible lining package assembly can well fit the synchronous bending of the profile, and has a good foiling effect on the profile, and is not prone to breakage and excessive bending that is difficult to restore.
以下结合图和实施例对本发明作进一步描述。The present invention will be further described below with reference to figures and embodiments.
附图说明Description of drawings
图1为薄壁开口型材拉弯工序工装总成的结构示意图;Fig. 1 is the structural schematic diagram of the tooling assembly in the drawing and bending process of thin-walled open profiles;
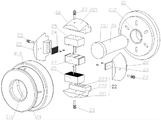
图2为夹头装置的爆炸图;Figure 2 is an exploded view of the chuck device;
图3为夹头装置的装配图;Fig. 3 is the assembly drawing of the collet device;
图4为夹头装置中的端部内衬块的结构示意图;Fig. 4 is the structural schematic diagram of the end lining block in the chuck device;
图5为薄壁开口型材与柔性衬包组件装配后的爆炸图;Figure 5 is an exploded view of the thin-walled opening profile and the flexible lining package assembly after assembly;
图6为图5的A部放大图;Fig. 6 is the enlarged view of A part of Fig. 5;
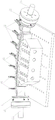
图7为薄壁开口型材与柔性衬包组件装配后的结构示意图;7 is a schematic structural diagram of the thin-walled opening profile and the flexible lining package assembly after assembly;
图8为侧壁夹持组件的结构示意图;8 is a schematic structural diagram of a side wall clamping assembly;
图9为本发明的工作状态示意图;Fig. 9 is the working state schematic diagram of the present invention;
图10为薄壁开口型材拉弯后的结构示意图。Fig. 10 is a schematic diagram of the structure of the thin-walled open profile after being stretched and bent.
说明:图3中的外壳沿轴向方向进行了剖切处理,以便于展示外壳内部各部件的装配关系。Description: The housing in Fig. 3 is cut along the axial direction in order to show the assembly relationship of the components inside the housing.
图例说明:薄壁开口型材1;U形槽11;翻边12;外壳21;型材装取口211;动力接入口212;连接座22;凸弧面221;安装面222;插接部A223;弹簧螺栓23;压块A24;压块B25;动力轴26;插接部B261;端部内衬块27;间隙270;插槽271;缺口272;中部柔性内衬31;辅助变形槽A311;中部包口外衬32;内侧槽321;外侧槽322;辅助变形槽B323;大力钳41;垫块42。Legend description: thin-walled open profile 1;
具体实施方式Detailed ways
实施例1:Example 1:
如图1-9所示,薄壁开口型材拉弯工序工装总成,包括薄壁开口型材1、夹头装置、柔性衬包组件和侧壁夹持组件。As shown in Figures 1-9, the tooling assembly for the thin-walled open profile drawing and bending process includes the thin-walled open profile 1, a collet device, a flexible lining package assembly and a side wall clamping assembly.
薄壁开口型材1上设有U形槽11,U形槽11一端封闭,另一端开口,开口处的两边沿向开口外侧翻展而形成翻边12。The thin-walled open profile 1 is provided with a
两组夹头装置分别用于夹持薄壁开口型材1的两端。夹头装置包括外壳21、连接座22、弹簧螺栓23、压块A24、压块B25、动力轴26和端部内衬块27。The two sets of clamping devices are respectively used to clamp both ends of the thin-walled opening profile 1 . The collet device includes a
外壳21呈套筒形,其内孔壁面为锥面,其两端分别设有连通至外壳21内孔的型材装取口211和动力接入口212,其外圆面上环形均布有四个连通至外壳内孔的腰形孔213,腰形孔213的延伸方向平行于外壳21轴向方向。The
连接座22一侧设有用于贴合外壳21内孔壁面的凸弧面221,连接座22另一侧设有安装面222和插接部A223。四个连接座22呈环形均布在外壳21内孔中,并呈两两相对布置。One side of the connecting
弹簧螺栓23头部一端位于外壳21外部,弹簧螺栓23杆部一端穿过外壳21上的腰形孔213,而伸入外壳21内孔中,并与连接座22螺纹连接。弹簧螺栓22通过弹力迫使连接座22的凸弧面221压紧在外壳21内孔壁面上。弹簧螺栓23的数量为四个,四个弹簧螺栓23分别与四个连接座22螺纹连接。One end of the head of the
两个压块A24可拆卸连接在其中两个相对布置的连接座23的安装面232上,并相对布置。两个压块B25可拆卸连接在另外两个相对布置的连接座23的安装面232上,并相对布置。两个压块A24与两个压块B25合围形成容纳区间,容纳区间与外壳21的型材装取口211直接连通。The two pressing blocks A24 are detachably connected to the mounting surfaces 232 of the two oppositely arranged
动力轴26活动安装在外壳21的动力接入口212上,其前端伸出在外壳21外部,以接收外部动力,其后端伸入外壳21内腔,其后端设有插接部B261。动力轴26通过插接部B261与四个连接座22的插接部A223活动插接。动力轴26在外部动力的驱动下沿外壳21轴向方向做往复直线运动,进而通过插接部B261与插接部A223的插接结构带动四个连接座22沿外壳21内孔壁面同步移动,以扩大或缩小容纳区间。The
端部内衬块27上设有两个相对的侧立面和设在两个侧立面之间的上、下端面,端部内衬块27上还设有两条贯通上、下端面的插槽271,端部内衬块27的下端面两侧分别设有缺口272。端部内衬块27活动安装在容纳区间内,其两个侧立面被夹紧在两个压块A24之间,其上端面与压块B25之间形成间隙270。两条插槽271在上端分别连通至间隙270的两侧,两条插槽271在下端各与一个缺口272连通,从而使间隙270、插槽271、缺口272依次连通而形成与薄壁开口型材1形状相适应的夹持区间。The
柔性衬包组件安装在薄壁开口型材1上,并位于薄壁开口型材1在两个夹头装置之间的长度段上。柔性衬包组件包括中部柔性内衬31和中部包口外衬32。The flexible liner pack assembly is mounted on the thin-walled opening profile 1 and is located on the length of the thin-walled opening profile 1 between the two collet devices. The flexible lining bag assembly includes a middle flexible
中部柔性内衬31为条形构件,其活动安装在薄壁开口型材1的U形槽11中,并与薄壁开口型材1的U形槽11的形状相适应。定义中部柔性内衬31与U形槽11底部正对的一侧表面为面A,定义中部柔性内衬31朝向U形槽11开口的一侧表面为面B,定义中部柔性内衬31正对U形槽11两侧壁的表面为面C。中部柔性内衬31上沿长度方向间隔设有多条辅助变形槽A311,辅助变形槽A311从面B向面A延伸,并将两个面C贯通。The middle flexible
中部包口外衬32为条形构件,其一侧表面上设有沿长度方向延伸且槽深由深至浅依次布置的内侧槽321和外侧槽322,外侧槽322设在内侧槽321的外部并将内侧槽321包容在内。中部包口外衬32一方面通过内侧槽321与中部柔性内衬31活动插接,另一方面通过外侧槽322将薄壁开口型材1开口及两翻边12包容在内。定义中部包口外衬32设有内侧槽321和外侧槽322的一侧表面为面D,定义中部包口外衬32与面D相对的一侧表面为面E,定义中部包口外衬32设在面D与面E之间并平行于中部包口外衬32长度方向的两个侧立面为面F。中部包口外衬32上沿长度方向间隔设有多条辅助变形槽B323,辅助变形槽B323从面D向面E延伸,并将两个面F贯通。The
多组侧壁夹持组件沿薄壁开口型材1的长度方向间隔安装在薄壁开口型材1上,并位于薄壁开口型材1在两个夹头装置之间的长度段上。侧壁夹持组件包括大力钳41和分别焊接在大力钳41两个钳嘴处的垫块42。大力钳41通过两个垫块42活动装夹在薄壁开口型材1的两面相对的外侧壁面上。Multiple sets of side wall clamping assemblies are installed on the thin-walled opening profile 1 at intervals along the length direction of the thin-walled opening profile 1, and are located on the length of the thin-walled opening profile 1 between the two clamping devices. The side wall clamping assembly includes a
优选,插接部A223为设在连接座22上的定位孔,插接部B261为设在动力轴26后端的圆柱凸台,所述圆柱凸台的形状与所述定位孔的形状相适应,从而实现插接部A223与插接部B261的活动插接。Preferably, the plug portion A223 is a positioning hole provided on the connecting
优选,外壳21为两段式分体结构,型材装取口211和动力接入口212分别设在外壳21的两段分体上。基于该结构,便于外壳21内部部件的装配和拆卸。Preferably, the
优选,两个压块A24分别在相对布置的表面上设有纵横交错的防滑纹路。Preferably, the two pressing blocks A24 are respectively provided with criss-crossing anti-skid textures on the oppositely arranged surfaces.
优选,两个压块B25分别在相对布置的表面上设有纵横交错的防滑纹路。Preferably, the two pressing blocks B25 are respectively provided with criss-cross anti-skid lines on the surfaces arranged oppositely.
优选,端部内衬块27的缺口272深度与薄壁开口型材1的翻边12厚度相适应;当薄壁开口型材1装夹在夹持区间内时,端部内衬块27的下端面与薄壁开口型材1的两个翻边12齐平。Preferably, the depth of the
本发明用于薄壁开口型材拉弯工序的装夹固定,装夹固定方法如下:The present invention is used for clamping and fixing in the drawing and bending process of thin-walled open profiles, and the clamping and fixing method is as follows:
S01,对薄壁开口型材进行充填及包口:S01, filling and wrapping thin-walled opening profiles:
1、将中部柔性内衬31安装在薄壁开口型材1的U形槽11中,安装到位后,中部柔性内衬31位于U形槽11的中部区段,中部柔性内衬31的面A与U形槽11底部正对并贴合,中部柔性内衬31的两个面C分别与U形槽11两侧壁正对并贴合;1. Install the middle
2、将中部包口外衬32安装在薄壁开口型材1的U形槽11开口处,并确保其与中部柔性内衬31的位置相对,一方面其通过内侧槽321与中部柔性内衬31活动插接,另一方面其通过外侧槽322将薄壁开口型材1的开口及两翻边12包容在内,再一方面其通过外侧槽322与内侧槽321之间的台阶面与薄壁开口型材1的两翻边12贴合;2. Install the
3、将两个端部内衬块27分别安装在薄壁开口型材1的两端,从而对薄壁开口型材1的U形槽11两端进行填充,安装到位后,薄壁开口型材1的U型槽11两侧壁分别穿过端部内衬块27的两条插槽271,端部内衬块27通过两条插槽271之间的区域将U形槽11填充。3. Install the two end lining blocks 27 on the two ends of the thin-walled open profile 1 respectively, so as to fill the two ends of the
本步骤完成时,薄壁开口型材1的U形槽11的全长被中部柔性内衬31和两个端部内衬块27填充满。When this step is completed, the entire length of the
S02,将夹头装置调节至初始状态:S02, adjust the chuck device to the initial state:
1、将两组夹头装置的动力轴26前端分别与拉弯机的动力输出部件连接,并控制拉弯机的动力输出部件动作,使两组夹头装置相互正对布置,并处在相距最远的距离;1. Connect the front ends of the
2、驱动动力轴26沿外壳21轴向方向移动,进而通过动力轴26的插接部B261与四个连接座22的插接部A223的配合关系,带动四个连接座22沿外壳21内孔壁面同步移动,将容纳区间扩大至极限;2. Drive the
本步骤中,拉弯机的动力输出部件一方面用于驱动动力轴26做水平直线移动,另一方面用于驱动夹头装置做水平弧形轨迹摆动和/或水平直线移动和/或竖向直线移动。In this step, on the one hand, the power output part of the stretch bender is used to drive the
S03,装夹固定薄壁开口型材:S03, clamping and fixing thin-walled opening profiles:
1、将进行了充填和包口的薄壁开口型材1吊至水平,并使其两端分别正对两个夹头装置的型材装取口211;1. Lift the thin-walled open profile 1 that has been filled and wrapped to the level, and make its two ends face the profile loading and unloading
2、控制拉弯机的动力输出部件动作,使两组夹头装置做相向水平直线移动,从而使薄壁开口型材的两端分别通过两个夹头装置的型材装取口211伸入两个夹头装置的容纳区间中;2. Control the action of the power output part of the stretch-bender, so that the two sets of collet devices move horizontally and linearly toward each other, so that the two ends of the thin-walled open profiles extend into the two parts through the profile loading and unloading
3、控制拉弯机的动力输出部件动作,驱动动力轴沿外壳21轴向方向移动,进而通过动力轴26的插接部B261与四个连接座22的插接部A223的配合关系,带动四个连接座22沿外壳21内孔壁面同步移动,将容纳区间缩小,直至夹紧薄壁开口型材1的端部;3. Control the action of the power output component of the stretch bender, drive the power shaft to move in the axial direction of the
4、将多组侧壁夹持组件沿薄壁开口型材1的长度方向间隔安装在薄壁开口型材1上,具体是将大力钳41调整为夹紧状态,从而使连接在大力钳41两个钳嘴上的垫块42压紧在薄壁开口型材1的两面相对的外侧壁面上。4. Install multiple sets of side wall clamping assemblies on the thin-walled opening profile 1 at intervals along the length direction of the thin-walled opening profile 1. Specifically, adjust the
本步骤中,两组相邻的侧壁夹持组件之间的间距应在满足下述条件的前提下取最小值;所述条件为:在薄壁开口型材1拉弯过程中,两组相邻的侧壁夹持组件不产生干涉。In this step, the distance between the two groups of adjacent side wall clamping components should take the minimum value under the premise of satisfying the following conditions; Adjacent sidewall clamping assemblies do not interfere.
本步骤完成时,薄壁开口型材1被两个夹头装置共同夹持,两个压块A分别压紧端部内衬块的两个侧立面,位于上端的压块B25通过其下表面压紧薄壁开口型材的封闭端外壁面,位于下端的压块B25通过其上表面压紧薄壁开口型材1的两翻边12及端部内衬块27的下端面。When this step is completed, the thin-walled open profile 1 is jointly clamped by two clamping devices, the two pressing blocks A press the two side elevations of the end lining block respectively, and the pressing block B25 at the upper end passes through its lower surface Press the outer wall surface of the closed end of the thin-walled open profile, and the pressing block B25 at the lower end presses the two
Claims (5)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210478442.1A CN114789210B (en) | 2022-05-05 | 2022-05-05 | Clamping and fixing method for thin-walled open profile bending process |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210478442.1A CN114789210B (en) | 2022-05-05 | 2022-05-05 | Clamping and fixing method for thin-walled open profile bending process |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN114789210A true CN114789210A (en) | 2022-07-26 |
| CN114789210B CN114789210B (en) | 2025-06-06 |
Family
ID=82461830
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210478442.1A Active CN114789210B (en) | 2022-05-05 | 2022-05-05 | Clamping and fixing method for thin-walled open profile bending process |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114789210B (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115815379A (en) * | 2022-09-28 | 2023-03-21 | 西安西部新锆科技股份有限公司 | Stretch bending die and stretch bending method for profile with Y-shaped section |
| CN117340079A (en) * | 2023-10-24 | 2024-01-05 | 珠海中联幕墙装饰工程有限公司 | Shaping mold for small radius aluminum profile and its bending method |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH461756A (en) * | 1965-05-03 | 1968-08-31 | Emil Dr Tobler | Process for the production of windows, window produced by this process and device for carrying out the process |
| CN108856526A (en) * | 2018-09-04 | 2018-11-23 | 沈阳飞机工业(集团)有限公司 | A kind of positioning flexible jig of stretch bending mold |
| CN111266444A (en) * | 2020-03-11 | 2020-06-12 | 广东高谱弯曲技术有限公司 | A high-precision double-arm bending machine |
| CN213591478U (en) * | 2020-09-07 | 2021-07-02 | 优靓重工(武汉)有限公司 | Novel profile bending machine |
| CN113070405A (en) * | 2021-05-08 | 2021-07-06 | 南华大学 | Section stretch bending die with replaceable template piece and assembling method thereof |
-
2022
- 2022-05-05 CN CN202210478442.1A patent/CN114789210B/en active Active
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH461756A (en) * | 1965-05-03 | 1968-08-31 | Emil Dr Tobler | Process for the production of windows, window produced by this process and device for carrying out the process |
| CN108856526A (en) * | 2018-09-04 | 2018-11-23 | 沈阳飞机工业(集团)有限公司 | A kind of positioning flexible jig of stretch bending mold |
| CN111266444A (en) * | 2020-03-11 | 2020-06-12 | 广东高谱弯曲技术有限公司 | A high-precision double-arm bending machine |
| CN213591478U (en) * | 2020-09-07 | 2021-07-02 | 优靓重工(武汉)有限公司 | Novel profile bending machine |
| CN113070405A (en) * | 2021-05-08 | 2021-07-06 | 南华大学 | Section stretch bending die with replaceable template piece and assembling method thereof |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115815379A (en) * | 2022-09-28 | 2023-03-21 | 西安西部新锆科技股份有限公司 | Stretch bending die and stretch bending method for profile with Y-shaped section |
| CN117340079A (en) * | 2023-10-24 | 2024-01-05 | 珠海中联幕墙装饰工程有限公司 | Shaping mold for small radius aluminum profile and its bending method |
Also Published As
| Publication number | Publication date |
|---|---|
| CN114789210B (en) | 2025-06-06 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US6912884B2 (en) | Hydroforming process and apparatus for the same | |
| HUP0002702A2 (en) | Method and apparatus for forming an oval cross-section and pipe form metal member | |
| CN114789210B (en) | Clamping and fixing method for thin-walled open profile bending process | |
| WO2002032596A1 (en) | Apparatus and method for hydroforming a tubular part | |
| CN117619984A (en) | A water swelling forming machine for stainless steel pipe processing | |
| CN114713683A (en) | Thin-walled open profile drawing and bending process tooling assembly | |
| US7797806B2 (en) | Internal high-pressure shaping method for shaping conical tubes made of metal | |
| JP5182426B2 (en) | Hydroform molding method and hydroform molding apparatus | |
| CN110935781A (en) | Novel interior high pressure forming die and shaping device | |
| CN111283105B (en) | Central air conditioning alloy connecting pipe fitting processing die | |
| CN211539141U (en) | Expanding mechanism and expanding machine using same | |
| CN114292993B (en) | Device for eliminating residual stress of forging | |
| CN219683857U (en) | High-pressure valve body forming die for power station | |
| CN112474899A (en) | Rubber plastic soft mold correction device and method for multi-cavity special-shaped double-layer thin-wall section pipe | |
| JP3514159B2 (en) | Hydraulic bulging apparatus for metal pipe and method for manufacturing metal pipe | |
| CN218556085U (en) | Frock clamp based on automobile parts welding | |
| CN111545640B (en) | An adjustable stamping die | |
| US6089064A (en) | Sliding plug for applying end loads during isostatic bulge forming | |
| CN110883157B (en) | A processing technology and device for double-head angle adjuster of automobile seat | |
| CN220462099U (en) | Sound insulation device for forging and pressing | |
| KR20050029092A (en) | Method and apparatus for manufacturing shell nut | |
| CN108709692B (en) | A aerating device for pipeline gas tightness detects | |
| CN224222452U (en) | Bulging integrated device with parallel double branch pipes | |
| CN218801803U (en) | Clamping device | |
| CN213918338U (en) | Vernier caliper claw deformation device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |