CN114770140A - Device and method for producing and assembling nameplate of electric energy meter - Google Patents
Device and method for producing and assembling nameplate of electric energy meter Download PDFInfo
- Publication number
- CN114770140A CN114770140A CN202210577836.2A CN202210577836A CN114770140A CN 114770140 A CN114770140 A CN 114770140A CN 202210577836 A CN202210577836 A CN 202210577836A CN 114770140 A CN114770140 A CN 114770140A
- Authority
- CN
- China
- Prior art keywords
- nameplate
- moving
- electric energy
- energy meter
- labeling
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P23/00—Machines or arrangements of machines for performing specified combinations of different metal-working operations not covered by a single other subclass
- B23P23/06—Metal-working plant comprising a number of associated machines or apparatus
Landscapes
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Labeling Devices (AREA)
Abstract
The invention discloses a device and a method for producing and assembling a nameplate of an electric energy meter. The production and assembly device comprises a rack and a transportation line which is arranged on the front side of the rack and used for transporting the electric energy meter; the label pasting machine further comprises a feeding mechanism, a code scanning device, a first moving device, a code carving device, a second moving device, a mounting manipulator and a label pasting device which are arranged on the machine frame. The automatic label inserting machine realizes the automatic operation of loading, code carving, labeling, overturning and mounting of a label, improves the production efficiency, and simultaneously solves the technical problem that a soft label cannot be accurately inserted into a clamping groove through a conventional manipulator.
Description
Technical Field
The invention relates to a device for producing and assembling a nameplate on an electric energy meter, and also relates to a method for producing and installing the nameplate of the electric energy meter.
Background
Be provided with the data plate that is used for the sign on the electric energy meter, need install the inboard of apron with the data plate before leaving the factory.
The nameplate in the electric energy meter is flexible. Generally will be through processes such as sign indicating number, subsides mark, place its rear side draw-in groove of apron through manual operation mode at last, complex operation, inefficiency, often because the misoperation can't be with in the correct card income draw-in groove of data plate moreover.
Disclosure of Invention
The invention provides a device and a method for producing and assembling a nameplate of an electric energy meter, and the purpose is that: (1) the automatic operation of nameplate production and tray loading is realized, and the production efficiency of the electric energy meter is improved; (2) ensure that the nameplate can be correctly clamped into the clamping groove.
The technical scheme of the invention is as follows:
an electric energy meter nameplate production and assembly device comprises a rack and a conveying line which is arranged on the front side of the rack and used for conveying electric energy meters;
the automatic labeling machine also comprises a feeding mechanism, a code scanning device, a first moving device, a code carving device, a second moving device, a mounting manipulator and a labeling device which are arranged on the rack;
the feeding mechanism is used for placing blank nameplates on the first mobile device;
the first mobile device is used for conveying blank nameplates to the code carving station;
the code engraving device is used for engraving a two-dimensional code for a blank nameplate of the code engraving station;
the code scanning device is used for scanning the two-dimensional code engraved on the nameplate;
the labeling device is used for labeling RFID (radio frequency identification devices) stickers on nameplates on a labeling station;
the second moving device is used for driving the nameplate to move between the code engraving station and the labeling station;
the mounting manipulator is used for placing the nameplate subjected to code carving and labeling into the electric energy meter;
still be provided with the location switching device on the transportation line for realize the location of electric energy meter and the switching of electric energy meter upper cover plate.
As a further improvement of the electric energy meter nameplate production and assembly device: the feeding mechanism comprises a machine body arranged on the rack, a vertical feeding groove is arranged on the machine body, the nameplate is horizontally stacked in the feeding groove, and a window is arranged at the bottom of the feeding groove;
the machine body is also provided with a first turnover mechanism, a rotating end of the first turnover mechanism is provided with a first telescopic mechanism, and a moving end of the first telescopic mechanism is provided with a first sucker for penetrating through the window to suck the nameplate at the bottommost part in the feeding groove;
a discharge port is formed in the bottom of the machine body, and a space is reserved between the bottom of the discharge port and the table board of the rack;
the first moving device comprises a first transverse moving mechanism arranged on the rack and a first carrying platform which moves left and right under the driving of the first transverse moving mechanism, and the first carrying platform is used for carrying a nameplate falling from the discharge port when moving to the lower part of the discharge port.
As a further improvement of the electric energy meter nameplate production and assembly device: and the third moving device is used for transferring the nameplate from the second moving device to the mounting manipulator.
As a further improvement of the electric energy meter nameplate production and assembly device: the second moving device comprises a second longitudinal moving mechanism, a second transverse moving mechanism, a second telescopic mechanism, a second turnover mechanism and a second sucker;
the second longitudinal moving mechanism is installed on the frame, the second transverse moving mechanism is installed at the moving end of the second longitudinal moving mechanism, the second telescopic mechanism is vertically arranged and installed at the moving end of the second transverse moving mechanism, the second turnover mechanism is installed at the moving end and the rotating axis of the second telescopic mechanism and is arranged in a front-back direction, and the second sucker is used for sucking a nameplate and is installed at the rotating end of the second turnover mechanism.
As a further improvement of the electric energy meter nameplate production and assembly device: the third moving device comprises a fourth longitudinal moving mechanism arranged on the rack and a second carrying platform moving back and forth under the driving of the fourth longitudinal moving mechanism;
the top of the second carrying platform is used for placing a nameplate; the second carrying platform horizontally extends out of the cantilever to the left, a U-shaped placing groove is formed in the top of the second carrying platform, and the left end of the placing groove is open; the bottom of the placing groove is also provided with a U-shaped groove which is communicated from top to bottom and moves from left to right, and the left end of the U-shaped groove is opened and is used for being matched with the second sucker.
As a further improvement of the electric energy meter nameplate production and assembly device: the mounting manipulator comprises a third transverse moving mechanism, a lifting mechanism, a third longitudinal moving mechanism and an operating mechanism;
the third transverse moving mechanism is installed on the rack, the lifting mechanism is installed at the moving end of the third transverse moving mechanism, the third longitudinal moving mechanism is installed at the moving end of the lifting mechanism, the operating mechanism is installed at the moving end of the third longitudinal moving mechanism, and the operating mechanism is used for holding and taking the nameplate.
As a further improvement of the electric energy meter nameplate production and assembly device: the operating mechanism comprises a body, and a push-down mechanism, a clamping mechanism and a third sucker are sequentially arranged on the body from left to right;
the push-down mechanism comprises a telescopic cylinder arranged on the body and a push roller arranged at the lower end of the telescopic cylinder, and the push roller is arranged in a front-back direction;
the clamping mechanism is provided with a front clamping jaw and a rear clamping jaw;
the push roller, the clamping jaw of the clamping mechanism and the third sucking disc are all located below the body.
As a further improvement of the electric energy meter nameplate production and assembly device: the positioning opening and closing device comprises a frame which is connected with a frame body of the transportation line through a lifting device and is positioned above the transportation line, and a clamping mechanism for fixing the electric energy meter is arranged on the frame; the frame is also provided with a third turnover mechanism, the tail end of the third turnover mechanism is provided with a fourth sucker, and the fourth sucker is used for being adsorbed on a cover plate of the electric energy meter;
the positioning opening and closing device further comprises a jacking device which is arranged on a frame body of the transportation line and used for lifting the electric energy meter.
As a further improvement of the electric energy meter nameplate production and assembly device: the labeling device is arranged below the table top of the rack and comprises a rack body, wherein a first winding wheel for placing an RFID sticker paper roll and a second winding wheel for placing a release paper roll separated from the RFID sticker paper roll are arranged on the rack body;
the frame body is also provided with a first roller way, a second roller way, a stripper, a labeling head, a labeling driving cylinder and a second code scanning gun;
the free end of the RFID sticker paper roll is connected to a stripper through a first roller way, release paper stripped by the stripper is wound to a second roll wheel through a second roller way, and a part which is remained after stripping and can be pasted is connected to a pasting head; the labeling driving cylinder is used for driving the labeling head to move up and down;
the second code scanning gun is used for scanning the two-dimensional code on the RFID sticker to be pasted;
a labeling window corresponding to the labeling head is formed in a labeling station on the table top of the rack; and a label reading device is arranged beside the labeling window and used for reading information in the RFID sticker during labeling.
The invention also discloses an electric energy meter nameplate production and assembly method, which is based on the electric energy meter nameplate production and assembly device and comprises the following specific steps:
Compared with the prior art, the invention has the following beneficial effects: (1) the automatic label loading, code carving, labeling, overturning and mounting operations are realized, and the production efficiency is obviously improved; (2) according to the invention, the third sucking disc, the clamping mechanism and the push roller are mutually matched, one side of the soft nameplate is inserted into the first clamping groove by using the sucking disc and the clamping mechanism, then the soft nameplate is slightly deformed by releasing the third sucking disc and pressing the push roller downwards, and finally the other side of the soft nameplate is inserted into the second clamping groove by using the reverse slight movement of the mounting manipulator, so that the problem that the soft nameplate cannot be accurately inserted into the clamping groove by using a conventional manipulator is solved; (3) according to the invention, through the two groups of code scanning guns and the one group of label reading device, whether the carved two-dimensional code, the RFID label information and the RFID surface two-dimensional code are unified or not can be automatically verified in the production process, so that the efficiency is further improved, and the workload of the later inspection link is reduced.
Drawings
FIG. 1 is a schematic view of the overall structure of the apparatus of the present invention
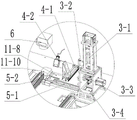
FIG. 2 is an enlarged view of a portion A of FIG. 1;
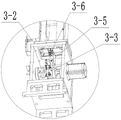
FIG. 3 is a bottom perspective view of the loading mechanism;
FIG. 4 is a schematic diagram of portions of a second mobile device and a third mobile device;
fig. 5 is a schematic view of a labeling apparatus;
FIG. 6 is a schematic view of a portion of the mounting robot and the positioning opening and closing device;
FIG. 7 is a schematic view of a portion of the operating mechanism;
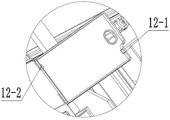
fig. 8 is a schematic diagram of a cover plate of the electric energy meter in an open state.
Detailed Description
The technical scheme of the invention is explained in detail in the following with the accompanying drawings:
the invention discloses a device and a method for producing and assembling a nameplate of an electric energy meter.
Referring to fig. 1, the nameplate production and assembly device for the electric energy meter comprises a frame 1 and a transportation line 2 arranged on the front side of the frame 1 and used for transporting the electric energy meter.
As shown in fig. 1 to 8, the electric energy meter nameplate production and assembly device further comprises a feeding mechanism 3, a code scanning device 4, a first moving device 5, a code carving device 6, a second moving device 7, a mounting manipulator 9 and a labeling device 11 which are mounted on the rack 1.
The feeding mechanism 3 is used to place blank nameplates onto the first moving device 5.
Specifically, as shown in fig. 2 and 3, the feeding mechanism 3 includes a machine body installed on the machine frame 1, a vertical feeding chute 3-1 is arranged on the machine body, a blank nameplate is horizontally stacked in the feeding chute 3-1, and a window is arranged at the bottom of the feeding chute 3-1.
The machine body is also provided with a first turnover mechanism 3-3, the first turnover mechanism 3-3 is driven by a motor, and a first telescopic mechanism 3-5 driven by a cylinder is arranged on a rotating end. The moving end of the first telescopic mechanism 3-5 is provided with a first sucker 3-6 which is used for penetrating through the open window to suck the nameplate at the bottommost part of the feeding groove 3-1.
And the side surface of the feeding groove 3-1 is also provided with a residual material sensor 3-2 for sensing a blank nameplate, and when the number of the nameplates is too small, an operator is prompted to supplement and place the nameplates in time.
The bottom of the machine body is provided with a discharge port 3-4, and a space is reserved between the bottom of the discharge port 3-4 and the table board of the machine frame 1.
The first moving device 5 is used for conveying blank nameplates to the code engraving station. The first moving device 5 comprises a first transverse moving mechanism 5-1 arranged on the frame 1 and a first carrying platform 5-2 which moves left and right under the driving of the first transverse moving mechanism 5-1. The first transverse moving mechanism 5-1 is driven by a cylinder. When the first carrying platform 5-2 moves to the position below the discharge port 3-4, the nameplate falling from the discharge port 3-4 is received, and then the nameplate is conveyed to the code engraving station at the left end.
Carve sign indicating number device 6 and be used for carving the two-dimensional code for the blank data plate of carving the sign indicating number station, use the sign indicating number equipment of carving among the prior art. The side of the code carving device 6 is provided with a smoking device for absorbing smoke dust generated during code carving.
The code scanning device 4 comprises a first longitudinal moving mechanism 4-1 and a first code scanning gun 4-2, wherein the first longitudinal moving mechanism 4-1 is driven by an air cylinder to control the first code scanning gun 4-2 to approach to and move away from the code marking device 6. The first code scanning gun 4-2 is used for scanning the two-dimensional code engraved on the nameplate.
As shown in fig. 4 and 6, the second moving device 7 is used for driving the nameplate to move between the coding station and the labeling station.
Specifically, the second moving device 7 comprises a second longitudinal moving mechanism 7-1, a second transverse moving mechanism 7-2, a second telescopic mechanism 7-3, a second turnover mechanism 7-4 and a second sucker 7-5.
The second longitudinal moving mechanism 7-1 is installed on the rack 1, is driven by a motor, and achieves linear movement through a lead screw guide rail mechanism. The second transverse moving mechanism 7-2 is arranged at the moving end of the second longitudinal mechanism and is also in a structure of a motor, a lead screw and a guide rail. The second telescopic mechanism 7-3 is vertically arranged, is arranged at the moving end of the second transverse moving mechanism 7-2 and is driven by an air cylinder. The second turnover mechanism 7-4 is arranged at the moving end of the second telescopic mechanism 7-3, and the rotation axis of the second turnover mechanism is arranged in the front-back direction and is driven by a motor. The second sucker 7-5 is used for sucking the nameplate and is arranged at the rotating end of the second turnover mechanism 7-4.
As shown in fig. 5, the labeling device 11 is used for attaching an RFID sticker to a nameplate at a labeling station.
The frame body is provided with a first winding wheel 11-1 for placing the RFID sticker paper roll and a second winding wheel 11-6 for placing the release paper roll separated from the RFID sticker paper roll, and the first winding wheel and the second winding wheel are driven by a motor to synchronously rotate.
The frame body is further provided with a first roller way 11-2, a second roller way 11-5, a stripper 11-3, a labeling head 11-4, a labeling driving cylinder 11-7 and a second code scanning gun 11-9.
The free end of the RFID sticker scroll is connected to a stripper 11-3 through a first roller way 11-2, release paper stripped by the stripper 11-3 is wound to a second roller way 11-6 through a second roller way 11-5, and a part capable of being pasted (provided with an RFID label and a two-dimensional code and having a pasting layer on the upward surface) left after stripping is connected to a pasting head 11-4. The labeling driving air cylinder 11-7 is used for driving the labeling head 11-4 to move up and down. The labeling head 11-4 realizes labeling when driving the sticker to move upwards.
And the second code scanning gun 11-9 is used for scanning the two-dimensional code on the RFID paster to be pasted.
As shown in fig. 2, a labeling window 11-8 corresponding to the position of the labeling head 11-4 is opened at a labeling station on the table top of the frame 1; and a label reading device 11-10 is arranged beside the labeling window 11-8, and the label reading device 11-10 is used for reading information in the RFID label paper during labeling. When the nameplate reaches the labeling window 11-8, the labeling head 11-4 moves upwards, and the RFID sticker is attached to the bottom of the nameplate.
As shown in fig. 4 and 6, the production assembly device further comprises third movement means 8 for transferring the name plate from the second movement means 7 to the mounting robot 9.
Specifically, the third moving device 8 includes a fourth longitudinal moving mechanism 8-1 mounted on the frame 1 and a second stage 8-2 moving back and forth under the driving of the fourth longitudinal moving mechanism 8-1.
The fourth longitudinal moving mechanism 8-1 adopts a structural form of a motor, a lead screw and a guide rail to realize linear movement.
The top of the second carrying platform 8-2 is used for placing a nameplate. Specifically, the second carrying platform 8-2 horizontally extends out of the cantilever to the left, a U-shaped placing groove is formed in the top of the second carrying platform, and the left end of the placing groove is open; the bottom of the placing groove is also provided with a vertically through U-shaped groove which runs left and right, and the left end of the U-shaped groove is open and is used for being matched with the second sucker 7-5.
The mounting manipulator 9 is used for placing a nameplate which finishes code carving and labeling into the electric energy meter.
Specifically, the mounting manipulator 9 comprises a third transverse moving mechanism 9-1, a lifting mechanism 9-2, a third longitudinal moving mechanism 9-3 and an operating mechanism 9-4.
The third transverse moving mechanism 9-1 is installed on the rack 1, the lifting mechanism 9-2 is installed at the moving end of the third transverse moving mechanism 9-1, the third longitudinal moving mechanism 9-3 is installed at the moving end of the lifting mechanism 9-2, and the operating mechanism 9-4 is installed at the moving end of the third longitudinal moving mechanism 9-3. The third transverse moving mechanism 9-1, the lifting mechanism 9-2 and the third longitudinal moving mechanism 9-3 all adopt a structural form of a motor-lead screw-guide rail to form an XYZ rectangular coordinate system mechanical arm, and drive the operating mechanism 9-4 to realize spatial movement.
As shown in figures 6 and 7, the operating mechanism 9-4 is used for holding nameplates and comprises a body, and a push-down mechanism 9-4-3, a clamping mechanism 9-4-2 and a third sucking disc 9-4-1 are sequentially arranged on the body from left to right.
The push-down mechanism 9-4-3 comprises a telescopic cylinder arranged on the body and a push roller arranged at the lower end of the telescopic cylinder, and the push roller is arranged in a front-back direction.
The clamping mechanism 9-4-2 is provided with a front clamping jaw and a rear clamping jaw, and is driven by an air cylinder to synchronously act so as to realize clamping and loosening.
The push roller, the clamping jaws of the clamping mechanism 9-4-2 and the third suction cup 9-4-1 are all positioned below the body.
As shown in fig. 1 and 6, a positioning opening and closing device 10 is further disposed on the transportation line 2, and is used for positioning the electric energy meter and opening and closing an upper cover plate 12 of the electric energy meter.
Specifically, the positioning opening and closing device 10 includes a frame 10-1 connected to the frame body of the transportation line 2 via a lifting device and located above the transportation line 2. The frame 10-1 is provided with a clamping mechanism for fixing the electric energy meter, and the clamping mechanism comprises a clamping cylinder, a positioning block and the like. The frame 10-1 is further provided with a third turnover mechanism 10-2, the third turnover mechanism 10-2 comprises a rotating rod driven by a motor, a fourth suction cup 10-3 is installed at the tail end of the rotating rod, and the fourth suction cup 10-3 is used for being adsorbed on a cover plate 12 of the electric energy meter.
The positioning opening and closing device 10 further comprises a jacking device which is installed on a frame body of the transportation line 2 and used for lifting the electric energy meter. The upper end of the jacking device is used for being matched with the electric energy meter or the bottom of a tray for loading the electric energy meter in a positioning mode.
The production and assembly method based on the electric energy meter nameplate production and assembly device comprises the following specific steps:
The feed mechanism 3 then returns to the initial position, awaiting the next tag to be picked up.
Then the first moving device 5 and the code scanning device 4 return to the initial position to wait for the next loading and code scanning.
Step 4, verifying and classifying: the control system verifies whether the two-dimensional code on the RFID sticker, the label information in the RFID sticker and the two-dimensional code carved in the step 2 are consistent or not; if the number plate is inconsistent with the standard plate, the second moving device 7 puts the number plate into a unqualified product station, the number plate leaves the rack 1 along the sliding groove, the subsequent steps are not executed, and the second moving device 7 returns to the original position to wait for sucking the next number plate which is just finished with the code carving; if so, the second mobile device 7 places a name plate on the second stage 8-2 of the third mobile device 8: the specific steps are that the second moving device 7 lifts up the nameplate and moves the nameplate to the left side of the second carrying platform 8-2 through the second longitudinal moving mechanism 7-1 and the second telescopic mechanism 7-3, then the second turnover mechanism 7-4 acts to enable the second sucking disc 7-5 and the nameplate to face upwards, then the second transverse moving mechanism 7-2 of the second moving device 7 acts to push the second sucking disc 7-5 into a U-shaped groove of the second carrying platform 8-2, then the second telescopic mechanism 7-3 enables the second sucking disc 7-5 and the nameplate to fall, the second sucking disc 7-5 is released, and the nameplate falls on the second carrying platform 8-2; then the second moving device 7 returns to the initial position to wait for sucking the next nameplate which is just engraved.
Step 6, placing a nameplate: a third sucking disc 9-4-1 of an operating mechanism 9-4 at the tail end of an installation manipulator 9 sucks a nameplate on a second carrier 8-2 from above (the second carrier 8-2 moves to a proper position in advance), then the clamping mechanism 9-4-2 clamps the front side and the rear side of the nameplate and moves the nameplate above a cover plate 12, the right end of the nameplate is close to a first clamping groove 12-1 on the right side, then the operating mechanism 9-4 moves to the right side, the right end of the nameplate is inserted into the first clamping groove 12-1 on the inner side of the cover plate 12, then the third sucking disc 9-4-1 on the right side of the clamping mechanism 9-4-2 is released, a push roller on the left side of the clamping mechanism 9-4-2 moves downwards to deform the left half part of the nameplate, then the operating mechanism 9-4 slightly moves to the left, the left end of the nameplate is inserted into a second clamping groove 12-2 on the inner side of the cover plate 12, finally the clamping mechanism 9-4-2 is released.
Claims (10)
1. The utility model provides an electric energy meter data plate production assembly quality which characterized in that: comprises a rack (1) and a transportation line (2) which is arranged at the front side of the rack (1) and is used for transporting an electric energy meter;
the automatic labeling machine further comprises a feeding mechanism (3), a code scanning device (4), a first moving device (5), a code carving device (6), a second moving device (7), a mounting manipulator (9) and a labeling device (11), wherein the feeding mechanism, the code carving device (6), the second moving device, the mounting manipulator and the labeling device are mounted on the rack (1);
the feeding mechanism (3) is used for placing blank nameplates on the first moving device (5);
the first moving device (5) is used for conveying a blank nameplate to the code carving station;
the code carving device (6) is used for carving a two-dimensional code for a blank nameplate of a code carving station;
the code scanning device (4) is used for scanning the two-dimensional code engraved on the nameplate;
the labeling device (11) is used for labeling RFID labels on nameplates on a labeling station;
the second moving device (7) is used for driving the nameplate to move between the code engraving station and the labeling station;
the mounting manipulator (9) is used for placing the nameplate which finishes the code carving and labeling into the electric energy meter;
the transportation line (2) is also provided with a positioning opening and closing device (10) for positioning the electric energy meter and opening and closing an upper cover plate (12) of the electric energy meter.
2. An electric energy meter nameplate production and assembly device as recited in claim 1, wherein: the feeding mechanism (3) comprises a machine body arranged on the rack (1), a vertical feeding groove (3-1) is formed in the machine body, the nameplate is horizontally stacked in the feeding groove (3-1), and a window is formed in the bottom of the feeding groove (3-1);
the machine body is also provided with a first turnover mechanism (3-3), a rotating end of the first turnover mechanism (3-3) is provided with a first telescopic mechanism (3-5), and a moving end of the first telescopic mechanism (3-5) is provided with a first sucker (3-6) which penetrates through the window to suck the nameplate at the bottommost part in the feeding groove (3-1);
a discharge port (3-4) is formed in the bottom of the machine body, and a space is reserved between the bottom of the discharge port (3-4) and the table top of the rack (1);
the first moving device (5) comprises a first transverse moving mechanism (5-1) installed on the rack (1) and a first carrying platform (5-2) moving left and right under the driving of the first transverse moving mechanism (5-1), and when the first carrying platform (5-2) moves to the position below the discharging port (3-4), the first carrying platform receives nameplates falling from the discharging port (3-4).
3. An electric energy meter nameplate production and assembly device as recited in claim 1, wherein: and third moving means (8) for transferring the name plate from the second moving means (7) to the mounting robot (9).
4. An electric energy meter nameplate production and assembly device as defined in claim 3, wherein: the second moving device (7) comprises a second longitudinal moving mechanism (7-1), a second transverse moving mechanism (7-2), a second telescopic mechanism (7-3), a second turnover mechanism (7-4) and a second sucker (7-5);
the second longitudinal moving mechanism (7-1) is installed on the rack (1), the second transverse moving mechanism (7-2) is installed at the moving end of the second longitudinal moving mechanism, the second telescopic mechanism (7-3) is vertically arranged and installed at the moving end of the second transverse moving mechanism (7-2), the second turnover mechanism (7-4) is installed at the moving end of the second telescopic mechanism (7-3) and is arranged in a front-back trend mode along the rotating axis, and the second sucker (7-5) is used for sucking a nameplate and is installed at the rotating end of the second turnover mechanism (7-4).
5. An electric energy meter nameplate production and assembly device as defined in claim 3, wherein: the third moving device (8) comprises a fourth longitudinal moving mechanism (8-1) arranged on the rack (1) and a second carrying platform (8-2) moving back and forth under the driving of the fourth longitudinal moving mechanism (8-1);
the top of the second carrying platform (8-2) is used for placing a nameplate; the second carrying platform (8-2) horizontally extends out of the cantilever to the left, a U-shaped placing groove is formed in the top of the second carrying platform, and the left end of the placing groove is open; the bottom of the placing groove is also provided with a U-shaped groove which is through from top to bottom and moves from left to right, and the left end of the U-shaped groove is open and is used for being matched with the second sucker (7-5).
6. An electric energy meter nameplate production and assembly device as set forth in claim 1, wherein: the mounting manipulator (9) comprises a third transverse moving mechanism (9-1), a lifting mechanism (9-2), a third longitudinal moving mechanism (9-3) and an operating mechanism (9-4);
the third transverse moving mechanism (9-1) is installed on the rack (1), the lifting mechanism (9-2) is installed at the moving end of the third transverse moving mechanism (9-1), the third longitudinal moving mechanism (9-3) is installed at the moving end of the lifting mechanism (9-2), the operating mechanism (9-4) is installed at the moving end of the third longitudinal moving mechanism (9-3), and the operating mechanism (9-4) is used for holding and taking the nameplate.
7. An electric energy meter nameplate production and assembly apparatus as set forth in claim 6, wherein: the operating mechanism (9-4) comprises a body, and a push-down mechanism (9-4-3), a clamping mechanism (9-4-2) and a third sucker (9-4-1) are sequentially arranged on the body from left to right;
the push-down mechanism (9-4-3) comprises a telescopic cylinder arranged on the body and a push roller arranged at the lower end of the telescopic cylinder, and the push roller is arranged in a front-back direction;
the clamping mechanism (9-4-2) is provided with a front clamping jaw and a rear clamping jaw;
the push roller, the clamping jaw of the clamping mechanism (9-4-2) and the third suction cup (9-4-1) are all positioned below the body.
8. An electric energy meter nameplate production and assembly device as set forth in claim 1, wherein: the positioning opening and closing device (10) comprises a frame (10-1) which is connected with a frame body of the transportation line (2) through a lifting device and is positioned above the transportation line (2), and a clamping mechanism for fixing the electric energy meter is arranged on the frame (10-1); the frame (10-1) is further provided with a third turnover mechanism (10-2), a fourth suction cup (10-3) is mounted at the tail end of the third turnover mechanism (10-2), and the fourth suction cup (10-3) is used for being adsorbed on a cover plate (12) of the electric energy meter;
the positioning opening and closing device (10) further comprises a jacking device which is arranged on a frame body of the transportation line (2) and used for lifting the electric energy meter.
9. An electric energy meter nameplate production and assembly device as recited in claim 1, wherein: the labeling device (11) is arranged below a table top of the rack (1) and comprises a rack body, wherein a first winding wheel (11-1) for placing an RFID sticker paper roll and a second winding wheel (11-6) for placing a release paper roll separated from the RFID sticker paper roll are arranged on the rack body;
the frame body is also provided with a first roller way (11-2), a second roller way (11-5), a stripper (11-3), a labeling head (11-4), a labeling driving cylinder (11-7) and a second code scanning gun (11-9);
the free end of the RFID sticker paper roll is connected to a stripper (11-3) through a first roller way (11-2), release paper stripped by the stripper (11-3) is wound to a second roll wheel (11-6) through a second roller way (11-5), and a part which can be pasted and is left after stripping is connected to a pasting head (11-4); the labeling driving cylinder (11-7) is used for driving the labeling head (11-4) to move up and down;
the second code scanning gun (11-9) is used for scanning a two-dimensional code on the RFID sticker to be pasted;
a labeling window (11-8) corresponding to the position of the labeling head (11-4) is formed in a labeling station on the table top of the rack (1); and a label reading device (11-10) is arranged beside the labeling window (11-8), and the label reading device (11-10) is used for reading information in the RFID sticker during labeling.
10. A production and assembly method for a nameplate of an electric energy meter is characterized by comprising the following steps: the method is based on the electric energy meter nameplate production and assembly device of claim 3, and comprises the following specific steps:
step 1, blank nameplate feeding: a first turnover mechanism (3-3) of the feeding mechanism (3) acts to enable a first sucker (3-6) to face upwards, then a first telescopic mechanism (3-5) of the feeding mechanism (3) extends, the first sucker (3-6) sucks the nameplate at the bottommost part in the feeding groove (3-1), then the first telescopic mechanism (3-5) retracts, the nameplate is taken out of the feeding groove (3-1) by the first sucker (3-6), the first turnover mechanism (3-3) acts to enable the first sucker (3-6) to face downwards, the first sucker (3-6) releases the sucked nameplate, and the nameplate falls onto a first carrying platform (5-2) of a first moving device (5);
step 2, code carving: the first moving device (5) moves the nameplate to a code carving station, the code carving device (6) starts to carve codes, and the carved two-dimensional codes are scanned through the code scanning device (4) to verify whether the codes are correct or not;
step 3, labeling: the nameplate is moved by a second moving device (7) to be provided with a labeling station, the RFID sticker is attached to the bottom of the nameplate through a labeling device (11), the two-dimensional code on the RFID sticker is scanned through a second code scanning gun (11-9), and the label information in the RFID sticker is read through a label reading device (11-10);
step 4, verifying and classifying: verifying whether the two-dimensional code on the RFID sticker, the label information in the RFID sticker and the two-dimensional code carved in the step 2 are consistent or not; if the two are inconsistent, the second moving device (7) puts the nameplate into a unqualified product station, and if the two are consistent, the second moving device (7) puts the nameplate onto a second carrying platform (8-2) of a third moving device (8): the nameplate is moved to the left side of the second carrying platform (8-2) by the second moving device (7), meanwhile, the second telescopic mechanism (7-3) and the second turnover mechanism (7-4) of the second moving device (7) act, the second sucking disc (7-5) and the nameplate of the second moving device (7) face upwards and are lifted, then the second transverse moving mechanism (7-2) of the second moving device (7) acts to push the second sucking disc (7-5) into the U-shaped groove of the second carrying platform (8-2), then the second telescopic mechanism (7-3) enables the second sucking disc (7-5) and the nameplate to fall, the second sucking disc (7-5) is released, and the nameplate falls onto the second carrying platform (8-2);
step 5, positioning and uncovering the electric energy meter: the jacking device of the positioning opening and closing device (10) jacks up the electric energy meter on the transportation line (2), then the lifting device of the positioning opening and closing device (10) drops the framework (10-1) to be sleeved outside the electric energy meter, and the clamping mechanism on the framework (10-1) acts to clamp and position the electric energy meter; a fourth sucking disc (10-3) on the frame (10-1) adsorbs a cover plate (12) of the electric energy meter, and then a third turnover mechanism (10-2) of the positioning opening and closing device (10) acts to open the cover plate (12);
step 6, placing a nameplate: a third sucking disc (9-4-1) of a tail end operating mechanism (9-4) of a mounting manipulator (9) sucks a nameplate on a second carrying platform (8-2) from the upper side, then the clamping mechanism (9-4-2) clamps the front side and the rear side of the nameplate, the nameplate is moved to the upper side of a cover plate (12), then the operating mechanism (9-4) moves to the right, the right end of the nameplate is inserted into a first clamping groove (12-1) in the inner side of the cover plate (12), then the third sucking disc (9-4-1) on the right side of the clamping mechanism (9-4-2) is released, a push roller on the left side of the clamping mechanism (9-4-2) moves downwards to deform the left half part of the nameplate, then the operating mechanism (9-4) moves to the left, the left end of the nameplate is inserted into a second clamping groove (12-2) in the inner side of the cover plate (12), finally, the clamping mechanism (9-4-2) is loosened;
step 7, closing the cover: and a third turnover mechanism (10-2) of the positioning opening and closing device (10) reversely acts to close the cover plate (12), the fourth sucker (10-3) releases the cover plate (12), then a clamping mechanism on the frame (10-1) is loosened, the lifting device lifts the frame (10-1), and the lifting device falls down to enable the electric energy meter to be placed on the transportation line (2) again.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210577836.2A CN114770140B (en) | 2022-05-25 | 2022-05-25 | Electric energy meter nameplate production and assembly device and method |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210577836.2A CN114770140B (en) | 2022-05-25 | 2022-05-25 | Electric energy meter nameplate production and assembly device and method |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN114770140A true CN114770140A (en) | 2022-07-22 |
| CN114770140B CN114770140B (en) | 2023-08-11 |
Family
ID=82407937
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210577836.2A Active CN114770140B (en) | 2022-05-25 | 2022-05-25 | Electric energy meter nameplate production and assembly device and method |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114770140B (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116275541A (en) * | 2022-12-19 | 2023-06-23 | 南京电力自动化设备三厂有限公司 | An engraving mechanism for an electric energy meter assembly system |
| CN121290066A (en) * | 2025-12-11 | 2026-01-09 | 杭州余杭獐山钢瓶有限公司 | A tooling for cutting and welding metal nameplates for steel cylinder covers |
| CN121290066B (en) * | 2025-12-11 | 2026-05-15 | 杭州余杭獐山钢瓶有限公司 | Integrative frock of metal nameplate cutting welding of steel bottle guard shield |
Citations (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH09290811A (en) * | 1996-04-26 | 1997-11-11 | Matsushita Electric Works Ltd | Automatic name plate affixing machine |
| CN105172382A (en) * | 2015-10-15 | 2015-12-23 | 苏州实创德光电科技有限公司 | Automatic nameplate laser code spraying device and using method thereof |
| KR20160000839U (en) * | 2014-09-02 | 2016-03-10 | 대우조선해양 주식회사 | Mounting Device for a Name Plate |
| CN107720395A (en) * | 2017-10-26 | 2018-02-23 | 江苏协昌电子科技股份有限公司 | The attachment mechanism of controller for electric vehicle sponge |
| CN207207459U (en) * | 2017-10-10 | 2018-04-10 | 武汉雷恩博激光科技有限公司 | A kind of nameplate automatic marking machine |
| CN108973366A (en) * | 2018-07-26 | 2018-12-11 | 广州凌绝顶智能设备有限公司 | A kind of automatic nameplate mark bending machine |
| CN208746460U (en) * | 2018-09-30 | 2019-04-16 | 许昌裕同印刷包装有限公司 | A kind of nameplate pastes machine |
| CN110127154A (en) * | 2019-05-15 | 2019-08-16 | 宁波三星智能电气有限公司 | A kind of ammeter dress name plate device |
| CN110181256A (en) * | 2019-05-15 | 2019-08-30 | 宁波三星智能电气有限公司 | A kind of full-automatic electricity meter dress name plate device |
| CN110589097A (en) * | 2019-10-10 | 2019-12-20 | 昆山萨满生物科技有限公司 | Packaging machine |
| CN110861815A (en) * | 2019-10-09 | 2020-03-06 | 广东贝贝机器人有限公司 | Labeling and code scanning device and labeling method for earphone packaging box |
| CN111112972A (en) * | 2019-12-20 | 2020-05-08 | 柏思齐 | A kind of automatic electric energy meter nameplate installation equipment and method |
| CN211162745U (en) * | 2019-12-09 | 2020-08-04 | 航天亮丽电气有限责任公司 | Automatic data plate installation equipment of electric energy meter |
| CN212364842U (en) * | 2020-05-20 | 2021-01-15 | 南斗六星系统集成有限公司 | Automatic change detection assembly line |
| CN215362259U (en) * | 2021-06-16 | 2021-12-31 | 郭贵元 | Electronic tag pasting machine based on automatic engraving of nameplate under ammeter |
| CN215658875U (en) * | 2021-09-22 | 2022-01-28 | 元启工业技术有限公司 | Device for quickly installing nameplate of electric energy meter on line |
| CN215753535U (en) * | 2020-12-25 | 2022-02-08 | 东方电气集团科学技术研究院有限公司 | Automatic labeling machine |
-
2022
- 2022-05-25 CN CN202210577836.2A patent/CN114770140B/en active Active
Patent Citations (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH09290811A (en) * | 1996-04-26 | 1997-11-11 | Matsushita Electric Works Ltd | Automatic name plate affixing machine |
| KR20160000839U (en) * | 2014-09-02 | 2016-03-10 | 대우조선해양 주식회사 | Mounting Device for a Name Plate |
| CN105172382A (en) * | 2015-10-15 | 2015-12-23 | 苏州实创德光电科技有限公司 | Automatic nameplate laser code spraying device and using method thereof |
| CN207207459U (en) * | 2017-10-10 | 2018-04-10 | 武汉雷恩博激光科技有限公司 | A kind of nameplate automatic marking machine |
| CN107720395A (en) * | 2017-10-26 | 2018-02-23 | 江苏协昌电子科技股份有限公司 | The attachment mechanism of controller for electric vehicle sponge |
| CN108973366A (en) * | 2018-07-26 | 2018-12-11 | 广州凌绝顶智能设备有限公司 | A kind of automatic nameplate mark bending machine |
| CN208746460U (en) * | 2018-09-30 | 2019-04-16 | 许昌裕同印刷包装有限公司 | A kind of nameplate pastes machine |
| CN110181256A (en) * | 2019-05-15 | 2019-08-30 | 宁波三星智能电气有限公司 | A kind of full-automatic electricity meter dress name plate device |
| CN110127154A (en) * | 2019-05-15 | 2019-08-16 | 宁波三星智能电气有限公司 | A kind of ammeter dress name plate device |
| CN110861815A (en) * | 2019-10-09 | 2020-03-06 | 广东贝贝机器人有限公司 | Labeling and code scanning device and labeling method for earphone packaging box |
| CN110589097A (en) * | 2019-10-10 | 2019-12-20 | 昆山萨满生物科技有限公司 | Packaging machine |
| CN211162745U (en) * | 2019-12-09 | 2020-08-04 | 航天亮丽电气有限责任公司 | Automatic data plate installation equipment of electric energy meter |
| CN111112972A (en) * | 2019-12-20 | 2020-05-08 | 柏思齐 | A kind of automatic electric energy meter nameplate installation equipment and method |
| CN212364842U (en) * | 2020-05-20 | 2021-01-15 | 南斗六星系统集成有限公司 | Automatic change detection assembly line |
| CN215753535U (en) * | 2020-12-25 | 2022-02-08 | 东方电气集团科学技术研究院有限公司 | Automatic labeling machine |
| CN215362259U (en) * | 2021-06-16 | 2021-12-31 | 郭贵元 | Electronic tag pasting machine based on automatic engraving of nameplate under ammeter |
| CN215658875U (en) * | 2021-09-22 | 2022-01-28 | 元启工业技术有限公司 | Device for quickly installing nameplate of electric energy meter on line |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116275541A (en) * | 2022-12-19 | 2023-06-23 | 南京电力自动化设备三厂有限公司 | An engraving mechanism for an electric energy meter assembly system |
| CN121290066A (en) * | 2025-12-11 | 2026-01-09 | 杭州余杭獐山钢瓶有限公司 | A tooling for cutting and welding metal nameplates for steel cylinder covers |
| CN121290066B (en) * | 2025-12-11 | 2026-05-15 | 杭州余杭獐山钢瓶有限公司 | Integrative frock of metal nameplate cutting welding of steel bottle guard shield |
Also Published As
| Publication number | Publication date |
|---|---|
| CN114770140B (en) | 2023-08-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110834931B (en) | Automatic assembly line of network terminal | |
| CN210338587U (en) | SMT (surface mount technology) tray high-speed automatic code reading and labeling equipment based on visual system | |
| CN216763496U (en) | PCB board integration sign processing equipment | |
| CN212526507U (en) | Efficient full-automatic laser marking device | |
| CN211418722U (en) | Automatic assembly line of network terminal | |
| CN109051151A (en) | Automatic labeling label apparatus | |
| CN219989721U (en) | An automated production line for cartoning and labeling | |
| CN106455353A (en) | Automatic PCB (Printed Circuit Board) high-temperature adhesive tearing device and adhesive tearing process thereof | |
| CN114760828B (en) | Keyboard backlight module processing detection connection system | |
| CN110919359A (en) | Automatic assembling method of network terminal | |
| CN210364732U (en) | Full-automatic double-station mobile phone shell labeling production line of continuous flow type | |
| CN111348236A (en) | Inductor and detection packaging equipment and method thereof | |
| CN108263701B (en) | Full-automatic labeling production system for PCB and implementation method | |
| CN114770140B (en) | Electric energy meter nameplate production and assembly device and method | |
| CN110683147A (en) | SMD material automatic labeling and boxing equipment | |
| CN218104072U (en) | Categorised balance device of charging tray | |
| CN116730001B (en) | A PCB board integrated marking processing equipment | |
| CN111348238A (en) | Inductor carrying device and method for inductor detection packaging equipment | |
| CN219468958U (en) | X-ray paster point material machine | |
| CN219996917U (en) | System for full-automatic detection FPC | |
| CN219295884U (en) | Novel automatic labeling machine for writing numbers | |
| CN115246509B (en) | Automatic labeling system and control method thereof | |
| CN223315391U (en) | Automatic wafer labeling machine | |
| CN116750296A (en) | An automated production line for cartoning and labeling | |
| CN210311252U (en) | Automatic labeling machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| TR01 | Transfer of patent right | ||
| TR01 | Transfer of patent right |
Effective date of registration: 20231107 Address after: No.6, Jindu Road, Laishan District, Yantai City, Shandong Province Patentee after: YANTAI DONGFANG WISDOM ELECTRIC Co.,Ltd. Patentee after: STATE GRID JIBEI ELECTRIC POWER Co.,Ltd. Address before: No.6, Jindu Road, Laishan District, Yantai City, Shandong Province Patentee before: YANTAI DONGFANG WISDOM ELECTRIC Co.,Ltd. |