CN114671672A - Formula and preparation method of unshaped refractory material - Google Patents
Formula and preparation method of unshaped refractory material Download PDFInfo
- Publication number
- CN114671672A CN114671672A CN202210354985.2A CN202210354985A CN114671672A CN 114671672 A CN114671672 A CN 114671672A CN 202210354985 A CN202210354985 A CN 202210354985A CN 114671672 A CN114671672 A CN 114671672A
- Authority
- CN
- China
- Prior art keywords
- rotating shaft
- grinding
- parts
- stirring
- built
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 239000011819 refractory material Substances 0.000 title claims abstract description 54
- 238000002360 preparation method Methods 0.000 title claims abstract description 14
- 238000009472 formulation Methods 0.000 title claims description 4
- 238000000227 grinding Methods 0.000 claims abstract description 88
- 238000003756 stirring Methods 0.000 claims abstract description 63
- 238000004519 manufacturing process Methods 0.000 claims abstract description 44
- 238000000034 method Methods 0.000 claims abstract description 33
- -1 magnesium aluminate Chemical class 0.000 claims abstract description 19
- 229910052596 spinel Inorganic materials 0.000 claims abstract description 19
- 239000011029 spinel Substances 0.000 claims abstract description 19
- 229910052749 magnesium Inorganic materials 0.000 claims abstract description 15
- 239000011777 magnesium Substances 0.000 claims abstract description 15
- PNEYBMLMFCGWSK-UHFFFAOYSA-N aluminium oxide Inorganic materials [O-2].[O-2].[O-2].[Al+3].[Al+3] PNEYBMLMFCGWSK-UHFFFAOYSA-N 0.000 claims abstract description 14
- 229910001570 bauxite Inorganic materials 0.000 claims abstract description 12
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 claims abstract description 9
- 229910026551 ZrC Inorganic materials 0.000 claims abstract description 9
- OTCHGXYCWNXDOA-UHFFFAOYSA-N [C].[Zr] Chemical compound [C].[Zr] OTCHGXYCWNXDOA-UHFFFAOYSA-N 0.000 claims abstract description 9
- 229910052814 silicon oxide Inorganic materials 0.000 claims abstract description 9
- CPLXHLVBOLITMK-UHFFFAOYSA-N magnesium oxide Inorganic materials [Mg]=O CPLXHLVBOLITMK-UHFFFAOYSA-N 0.000 claims abstract description 8
- 239000000395 magnesium oxide Substances 0.000 claims abstract description 7
- AXZKOIWUVFPNLO-UHFFFAOYSA-N magnesium;oxygen(2-) Chemical compound [O-2].[Mg+2] AXZKOIWUVFPNLO-UHFFFAOYSA-N 0.000 claims abstract description 6
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 claims abstract description 6
- KXGFMDJXCMQABM-UHFFFAOYSA-N 2-methoxy-6-methylphenol Chemical compound [CH]OC1=CC=CC([CH])=C1O KXGFMDJXCMQABM-UHFFFAOYSA-N 0.000 claims abstract description 5
- LFQSCWFLJHTTHZ-UHFFFAOYSA-N Ethanol Chemical compound CCO LFQSCWFLJHTTHZ-UHFFFAOYSA-N 0.000 claims abstract description 5
- 229920001568 phenolic resin Polymers 0.000 claims abstract description 5
- 239000005011 phenolic resin Substances 0.000 claims abstract description 5
- 239000004743 Polypropylene Substances 0.000 claims abstract description 4
- 229920001155 polypropylene Polymers 0.000 claims abstract description 4
- 239000002994 raw material Substances 0.000 claims description 40
- 239000011230 binding agent Substances 0.000 claims description 34
- 239000000843 powder Substances 0.000 claims description 19
- 239000000463 material Substances 0.000 claims description 18
- 229920001971 elastomer Polymers 0.000 claims description 10
- 239000004033 plastic Substances 0.000 claims description 10
- 229920003023 plastic Polymers 0.000 claims description 10
- 238000002156 mixing Methods 0.000 claims description 8
- 238000005303 weighing Methods 0.000 claims description 6
- 230000005540 biological transmission Effects 0.000 claims description 5
- 238000000926 separation method Methods 0.000 claims description 5
- 238000009826 distribution Methods 0.000 claims description 4
- 238000007580 dry-mixing Methods 0.000 claims description 3
- 239000000203 mixture Substances 0.000 claims 2
- 238000007599 discharging Methods 0.000 claims 1
- 230000008569 process Effects 0.000 abstract description 18
- 239000007767 bonding agent Substances 0.000 abstract description 8
- 238000005265 energy consumption Methods 0.000 abstract description 8
- 230000035939 shock Effects 0.000 abstract description 7
- 230000007797 corrosion Effects 0.000 abstract description 5
- 238000005260 corrosion Methods 0.000 abstract description 5
- 230000000694 effects Effects 0.000 description 7
- 238000005096 rolling process Methods 0.000 description 7
- 235000017166 Bambusa arundinacea Nutrition 0.000 description 5
- 235000017491 Bambusa tulda Nutrition 0.000 description 5
- 241001330002 Bambuseae Species 0.000 description 5
- 235000015334 Phyllostachys viridis Nutrition 0.000 description 5
- 239000011425 bamboo Substances 0.000 description 5
- 239000011449 brick Substances 0.000 description 4
- 239000002245 particle Substances 0.000 description 3
- 239000002893 slag Substances 0.000 description 3
- 230000008859 change Effects 0.000 description 2
- 238000010276 construction Methods 0.000 description 2
- 230000003628 erosive effect Effects 0.000 description 2
- 239000010977 jade Substances 0.000 description 2
- 230000035699 permeability Effects 0.000 description 2
- 230000002035 prolonged effect Effects 0.000 description 2
- 238000004904 shortening Methods 0.000 description 2
- 238000005245 sintering Methods 0.000 description 2
- 230000009471 action Effects 0.000 description 1
- 239000000654 additive Substances 0.000 description 1
- 230000000996 additive effect Effects 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000000903 blocking effect Effects 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 238000004134 energy conservation Methods 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
Images




Classifications
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/01—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics
- C04B35/10—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics based on aluminium oxide
- C04B35/101—Refractories from grain sized mixtures
- C04B35/103—Refractories from grain sized mixtures containing non-oxide refractory materials, e.g. carbon
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B02—CRUSHING, PULVERISING, OR DISINTEGRATING; PREPARATORY TREATMENT OF GRAIN FOR MILLING
- B02C—CRUSHING, PULVERISING, OR DISINTEGRATING IN GENERAL; MILLING GRAIN
- B02C15/00—Disintegrating by milling members in the form of rollers or balls co-operating with rings or discs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B02—CRUSHING, PULVERISING, OR DISINTEGRATING; PREPARATORY TREATMENT OF GRAIN FOR MILLING
- B02C—CRUSHING, PULVERISING, OR DISINTEGRATING IN GENERAL; MILLING GRAIN
- B02C23/00—Auxiliary methods or auxiliary devices or accessories specially adapted for crushing or disintegrating not provided for in preceding groups or not specially adapted to apparatus covered by a single preceding group
- B02C23/08—Separating or sorting of material, associated with crushing or disintegrating
- B02C23/16—Separating or sorting of material, associated with crushing or disintegrating with separator defining termination of crushing or disintegrating zone, e.g. screen denying egress of oversize material
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/622—Forming processes; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/626—Preparing or treating the powders individually or as batches ; preparing or treating macroscopic reinforcing agents for ceramic products, e.g. fibres; mechanical aspects section B
- C04B35/63—Preparing or treating the powders individually or as batches ; preparing or treating macroscopic reinforcing agents for ceramic products, e.g. fibres; mechanical aspects section B using additives specially adapted for forming the products, e.g.. binder binders
- C04B35/632—Organic additives
- C04B35/634—Polymers
- C04B35/63404—Polymers obtained by reactions only involving carbon-to-carbon unsaturated bonds
- C04B35/63408—Polyalkenes
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/622—Forming processes; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/626—Preparing or treating the powders individually or as batches ; preparing or treating macroscopic reinforcing agents for ceramic products, e.g. fibres; mechanical aspects section B
- C04B35/63—Preparing or treating the powders individually or as batches ; preparing or treating macroscopic reinforcing agents for ceramic products, e.g. fibres; mechanical aspects section B using additives specially adapted for forming the products, e.g.. binder binders
- C04B35/632—Organic additives
- C04B35/634—Polymers
- C04B35/63448—Polymers obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds
- C04B35/63472—Condensation polymers of aldehydes or ketones
- C04B35/63476—Phenol-formaldehyde condensation polymers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B02—CRUSHING, PULVERISING, OR DISINTEGRATING; PREPARATORY TREATMENT OF GRAIN FOR MILLING
- B02C—CRUSHING, PULVERISING, OR DISINTEGRATING IN GENERAL; MILLING GRAIN
- B02C23/00—Auxiliary methods or auxiliary devices or accessories specially adapted for crushing or disintegrating not provided for in preceding groups or not specially adapted to apparatus covered by a single preceding group
- B02C23/08—Separating or sorting of material, associated with crushing or disintegrating
- B02C23/16—Separating or sorting of material, associated with crushing or disintegrating with separator defining termination of crushing or disintegrating zone, e.g. screen denying egress of oversize material
- B02C2023/165—Screen denying egress of oversize material
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/32—Metal oxides, mixed metal oxides, or oxide-forming salts thereof, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3217—Aluminum oxide or oxide forming salts thereof, e.g. bauxite, alpha-alumina
- C04B2235/3222—Aluminates other than alumino-silicates, e.g. spinel (MgAl2O4)
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/34—Non-metal oxides, non-metal mixed oxides, or salts thereof that form the non-metal oxides upon heating, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3418—Silicon oxide, silicic acids or oxide forming salts thereof, e.g. silica sol, fused silica, silica fume, cristobalite, quartz or flint
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/38—Non-oxide ceramic constituents or additives
- C04B2235/3817—Carbides
- C04B2235/3839—Refractory metal carbides
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Materials Engineering (AREA)
- Structural Engineering (AREA)
- Organic Chemistry (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Inorganic Chemistry (AREA)
- Food Science & Technology (AREA)
- Furnace Housings, Linings, Walls, And Ceilings (AREA)
Abstract
The invention discloses a formula of an unshaped refractory material and a preparation method thereof, belonging to the technical field of unshaped refractory materials; the formula of the unshaped refractory material comprises aggregate and a bonding agent, wherein the aggregate comprises 20-35 parts of high alumina bauxite, 10-30 parts of magnesium aluminate spinel, 10-15 parts of silicon oxide, 5-20 parts of zirconium carbide and 3-8 parts of semisteel; the bonding agent comprises 12-26 parts of organic bonding agent, the organic bonding agent is random polypropylene or one or more of phenolic resin and absolute ethyl alcohol, the mass fraction of magnesium oxide in the magnesium aluminate spinel is 10-28%, and the mass fraction of aluminum oxide is 72-90%. According to the method, the formular is prepared by adopting production equipment of the unshaped refractory, and the processes of stirring and grinding are simultaneously completed on the basis of the formular refractory, so that the production process is simplified, the energy consumption is saved, and the unshaped refractory with good thermal shock stability, corrosion resistance and strong impermeability can be prepared.
Description
Technical Field
The invention relates to an unshaped refractory material and a preparation method thereof, in particular to a formula of an unshaped refractory material and a preparation method thereof, belonging to the technical field of refractory materials.
Background
The unshaped refractory material is a refractory material which is formed by mixing refractory aggregate with certain grain size distribution, powder, a bonding agent and an additive, and is also called as a bulk refractory material. It is used as lining of thermal equipment, and is directly roasted without sintering process. Compared with refractory bricks, the refractory bricks have the characteristics of simple process (saving sintering process), energy conservation, low cost, convenience for mechanized construction and the like. The effect of the refractory brick is better than that of the refractory brick in certain thermal equipment.
The refractory material used as the lining of the thermal equipment is affected by high temperature in the using process and is often accompanied with the erosion of slag or slag liquid gas, so the damage and erosion of the furnace lining are key factors influencing the service life of the furnace lining, the prior furnace lining material is generally required to be processed by a plurality of procedures of stirring and grinding a plurality of raw materials in the production process, most of the prior production equipment of the unshaped refractory material has single function and cannot simultaneously realize two operation processing of stirring and grinding, and the stirring and grinding steps are required to be completed separately in different equipment, so the production procedure of the unshaped refractory material is complex and causes higher energy consumption of the equipment, meanwhile, the aim of fully mixing can not be achieved in the conventional mixing and stirring process due to different particle sizes of the raw materials, the finished material has poor uniformity caused by the influence of the preparation process, further causes poor local corrosion resistance of the material, The slag resistance is poor, and the production quality is easily influenced.
Disclosure of Invention
The purpose of the invention is: the formula is prepared by adopting production equipment of the unshaped refractory material, and stirring and grinding processes are simultaneously completed on the basis of the formula of the unshaped refractory material, so that the production process is simplified, the energy consumption is saved, and meanwhile, the unshaped refractory material with good thermal shock stability, corrosion resistance and strong impermeability can be prepared.
In order to achieve the purpose, the invention adopts the following technical scheme: the formular of the unshaped refractory material comprises aggregate and a binding agent, wherein the aggregate comprises 20-35 parts of high-alumina bauxite, 10-30 parts of magnesia-alumina spinel, 10-15 parts of silicon oxide, 5-20 parts of zirconium carbide and 3-8 parts of semisteel; the binding agent comprises 12-26 parts of organic binding agent, wherein the organic binding agent adopts atactic polypropylene or one or more of phenolic resin and absolute ethyl alcohol.
The magnesium aluminate spinel contains 10-28% of magnesium oxide and 72-90% of aluminum oxide by mass.
The preferable mass ratio of the high bauxite to the magnesium aluminate spinel is 1: 1.
A method for preparing an unshaped refractory material comprises the following steps:
s1, weighing raw materials: respectively weighing aggregate and a binding agent according to the mass parts, and preparing by adopting production equipment of the unshaped refractory material;
s2, dry mixing, stirring and grinding: putting the weighed aggregate into a feeding port at the upper end of a processing box main body, and adjusting the feeding caliber through a movable baffle and a movable rod arranged at the lower end of the feeding port to control the feeding amount;
the aggregate enters a built-in barrel in the processing box main body after passing through a feeding hole, multi-stage stirring processing is carried out through a stirring plate and an inclined plate which are arranged in two layers in the built-in barrel, and the stirring time is controlled to be 3-12 min;
the aggregate flows out of the grinding roller after passing through the lower inclined plate, grinding and crushing of the aggregate are carried out through the grinding roller and the grinding blocks correspondingly arranged on the grinding plate at the lower end, the grinding time is 15-20min, the ground aggregate powder falls onto a guide plate at the bottom of the built-in cylinder through material leakage holes arranged on the grinding plate, the guide plate collects the aggregate powder and guides the aggregate powder out of a discharge hole at the lower end of the processing box main body, and finally the dry-mixed aggregate powder is obtained;
s3, forming of mixed binders: putting the obtained dry-mixed aggregate powder and the weighed binding agent into production equipment of the unshaped refractory again for preparation, wherein the mixing and stirring time of the dry-mixed aggregate powder and the binding agent is controlled to be 5-8min, and finally obtaining the unshaped refractory formed by combination after multi-stage stirring;
in the production equipment for the unshaped refractory material, the upper end and the lower end of the processing box main body are respectively provided with the feed inlet and the discharge outlet, the interior of the processing box main body is provided with the built-in barrel, and the interior of the built-in barrel is sequentially provided with the first rotating shaft, the second rotating shaft and the third rotating shaft from top to bottom; one ends of the first rotating shaft, the second rotating shaft and the third rotating shaft are connected with the inner wall of the built-in cylinder through bearings, the other ends of the first rotating shaft, the second rotating shaft and the third rotating shaft penetrate through the built-in cylinder in a sliding mode and are connected with the inner wall of the processing box main body through bearings, and one ends of the first rotating shaft, the second rotating shaft and the third rotating shaft, which are positioned outside the built-in cylinder, are connected with the same conveying belt through pulley transmission;
a motor for driving the third rotating shaft to rotate is arranged at the bottom end of the outer part of the processing box main body, and a plurality of stirring plates with hollow structures are fixed around the outer parts of the first rotating shaft and the second rotating shaft;
two layers of inclined plates which are distributed in a staggered manner are arranged at the upper end and the lower end in the built-in cylinder, the inclined plates are fixed on the inner wall of the built-in cylinder in a hollow structure, and the two layers of inclined plates are respectively positioned at intervals between the first rotating shaft and the second rotating shaft and between the second rotating shaft and the third rotating shaft;
a grinding roller is sleeved outside the third rotating shaft, and a grinding disc is arranged below the grinding roller; the two sides of the bottom wall of the built-in cylinder are both provided with guide plates, and the top surfaces of the guide plates are both of an inward inclined structure.
In the production equipment of the unshaped refractory material, baffles which are in circular arc structures are hinged to the inner walls of two sides of the feed inlet through rotating shafts, a groove is formed below the joint of the baffles and the inner walls of the feed inlet, a screw rod is connected to the inside of the groove through a bearing, a threaded sleeve is sleeved outside the screw rod through a threaded structure, a movable rod is connected between the outer side of the threaded sleeve and the bottom of the baffle, and two ends of the movable rod are respectively hinged to the outer side of the threaded sleeve and the bottom of the baffle; and the outside fixed cover on screw rod top is equipped with the plastics gear, the position that corresponds with the plastics gear on the diapire of recess is equipped with the opening.
In the production equipment of the unshaped refractory material, four stirring plates are arranged outside a first rotating shaft and a second rotating shaft, and the included angles between the stirring plates are 90 degrees; the top of hollow structure's stirring board is equipped with a plurality of through-hole, and the inside of stirring board is fixed with the separation blade that a plurality of is equidistant distribution to the outer end of stirring board is open structure.
In the production equipment of the unshaped refractory material, an elastic rubber layer is arranged between the inner wall of the grinding roller and the outer wall of the third rotating shaft, and the elastic rubber layer is of an annular structure.
In the production equipment of the unshaped refractory material, the top of the grinding disc is tightly attached to the bottom of the grinding roller, and a plurality of grinding blocks in semicircular structures are arranged at the top of the grinding disc and the outer part of the grinding roller; the border of grinding disc and the inner wall fixed connection of a built-in section of thick bamboo, just a plurality of hourglass material hole has been seted up to grinding disc's inside to hourglass material hole site is located the space department between the piece that rolls.
The invention has the beneficial effects that:
1) according to the formula, the high-alumina bauxite is matched with the magnesium aluminate spinel as a main aggregate, so that the overall strength of the refractory material is improved, and the thermal shock resistance and the permeability resistance of the refractory material are further improved by combining the silicon oxide, the zirconium carbide, the semisteel jade and the organic binder, so that the high-temperature volume structure of the material is more compact and stable.
2) The production equipment of the unshaped refractory material in the preparation method can complete the processes of stirring and grinding the raw materials simultaneously, and simplify the production process of the unshaped refractory material, thereby shortening the production period, reducing the production cost of the process and reducing the energy consumption; the production process is simplified, the energy consumption is saved, meanwhile, various raw materials with different particle sizes can be fully mixed through multi-stage stirring and grinding, and the unshaped refractory material with good thermal shock stability, strong corrosion resistance and strong impermeability is prepared, so that the service life of the furnace lining is prolonged, and the refractory quality of the furnace lining is improved.
Drawings
FIG. 1 is a schematic view showing the construction of an amorphous refractory manufacturing apparatus according to the present invention;
FIG. 2 is a schematic view of the interior of the feed gap of FIG. 1;
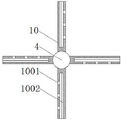
FIG. 3 is a schematic structural view of the connection between the first rotating shaft and the stirring plate in FIG. 1;
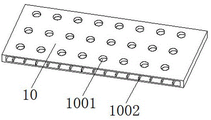
FIG. 4 is a schematic perspective view of the stirring plate of FIG. 1;
FIG. 5 is a schematic view of the third shaft of FIG. 1 connected to a grinding roll;
fig. 6 is a schematic view of the top of the crushing disk of fig. 1.
In the drawings, 1-the main body of the tank is processed; 2-a feed port, 201-a baffle, 202-a groove, 203-a screw, 204-a thread bush, 205-a movable rod, 206-a plastic gear; 3-a built-in cylinder; 4-a first rotating shaft; 5-a second rotating shaft; 6-a conveyor belt; 7-a third rotating shaft; 8, a motor; 9-inclined plates; 10-stirring plate; 1001-through hole; 1002-blocking piece; 11-grinding rollers; 12-grinding and briquetting; 13-rolling a disc; 14-a discharge hole; 15-a baffle; 16-an elastic rubber layer; 17-material leakage hole.
Detailed Description
The invention is further explained below with reference to the figures and the embodiments.
Example 1: the formula of the unshaped refractory material comprises aggregate and a bonding agent, wherein the aggregate comprises 20 parts of high alumina bauxite, 20 parts of magnesia-alumina spinel, 10 parts of silicon oxide, 15 parts of zirconium carbide and 6 parts of semisteel; the binding agent comprises 12 parts of organic binding agent, and the organic binding agent adopts 7 parts of phenolic resin and 5 parts of absolute ethyl alcohol.
The magnesia-alumina spinel contains 10% of magnesia and 90% of alumina.
The preparation method of the amorphous refractory material comprises the following steps:
s1, weighing raw materials: respectively weighing aggregate and a binding agent according to the mass parts, and preparing by adopting production equipment of the unshaped refractory material;
s2, dry mixing, stirring and grinding: the weighed aggregate is placed into a feeding hole 2 at the upper end of a processing box main body 1, and the feeding caliber is adjusted through a movable baffle 201 and a movable rod 205 arranged at the lower end of the feeding hole 2 to control the feeding amount;
the aggregate enters a built-in cylinder 3 in a processing box main body 1 through a feeding hole 2, and is subjected to multistage stirring processing through a stirring plate 10 and an inclined plate 9 which are arranged in two layers in the built-in cylinder 3, wherein the stirring time is controlled to be 3-12 min;
the aggregate flows out of a grinding roller 11 after passing through a lower inclined plate 9, grinding and crushing of the aggregate are carried out through a grinding roller 11 and a grinding block 12 correspondingly arranged on a lower-end grinding plate 13, the grinding time is 15-20min, the granularity range is 0.2-0.8mm, the ground aggregate powder falls onto a guide plate 15 at the bottom of a built-in cylinder 3 through a material leakage hole 17 arranged on the grinding plate 13, the guide plate 15 collects the aggregate powder and guides the aggregate powder out of a discharge hole 14 at the lower end of a processing box main body 1, and finally the dry-mixed aggregate powder is obtained;
s3, forming of mixed binders: and putting the obtained dry-mixed aggregate powder and the weighed binding agent into production equipment of the unshaped refractory again for preparation, wherein the mixing and stirring time of the dry-mixed aggregate powder and the binding agent is controlled to be 5-8min, and finally obtaining the unshaped refractory formed by combination after multi-stage stirring.
Example 2: in contrast to the embodiment 1, the process of the invention,
the formula of the unshaped refractory material comprises aggregate and a bonding agent, wherein the aggregate comprises 25 parts of high alumina bauxite, 10 parts of magnesia-alumina spinel, 12 parts of silicon oxide, 5 parts of zirconium carbide and 8 parts of semisteel; the binder comprises 18 parts of organic binder, and the organic binder is phenolic resin.
The mass fraction of magnesium oxide in the magnesium aluminate spinel is 15%, and the mass fraction of aluminum oxide is 85%.
Example 3: in contrast to the embodiment 1, the process of the invention,
the formular of the unshaped refractory material comprises aggregate and a binding agent, wherein the aggregate comprises 35 parts of high alumina bauxite, 30 parts of magnesium aluminate spinel, 15 parts of silicon oxide, 20 parts of zirconium carbide and 3 parts of semisteel; the binder comprises 26 parts of organic binder, and the organic binder adopts atactic polypropylene.
The mass fraction of magnesium oxide in the magnesium aluminate spinel is 20%, and the mass fraction of aluminum oxide is 80%.
Example 4: in contrast to the embodiment 1, the process of the invention,
the formula of the unshaped refractory material comprises aggregate and a bonding agent, wherein the aggregate comprises 30 parts of high alumina bauxite, 25 parts of magnesium aluminate spinel, 13 parts of silicon oxide, 10 parts of zirconium carbide and 5 parts of semisteel; the binding agent comprises 24 parts of organic binding agent and absolute ethyl alcohol of the organic binding agent.
The mass fraction of magnesium oxide in the magnesium aluminate spinel is 28%, and the mass fraction of aluminum oxide is 72%.
The physical and chemical indexes of the unshaped refractory materials prepared by the preparation method in the examples 1-4 are detected, and the detection result shows that the material in the example 1 has better thermal shock stability when the mass ratio of the bauxite to the magnesium aluminate spinel is 1: 1.
As shown in fig. 1-6, the above preparation method of an unshaped refractory material relates to a production apparatus of the unshaped refractory material, which comprises a processing box main body 1, wherein the upper end and the lower end of the processing box main body 1 are respectively provided with a feed inlet 2 and a discharge outlet 14, an inner barrel 3 is arranged inside the processing box main body 1, the upper end and the lower end of the inner barrel 3 are both welded and fixed with the inner wall of the processing box main body 1, and the inner barrel 3 is internally provided with a first rotating shaft 4, a second rotating shaft 5 and a third rotating shaft 7 in sequence from top to bottom; one ends of the first rotating shaft 4, the second rotating shaft 5 and the third rotating shaft 7 are connected with the inner wall of the built-in cylinder 3 through bearings, the other ends of the first rotating shaft 4, the second rotating shaft 5 and the third rotating shaft 7 slidably penetrate through the built-in cylinder 3 and are connected with the inner wall of the processing box main body 1 through bearings, rubber rings are arranged at the joints of the built-in cylinder 3 and the first rotating shaft 4, the second rotating shaft 5 and the third rotating shaft 7, and one ends of the first rotating shaft 4, the second rotating shaft 5 and the third rotating shaft 7, which are positioned outside the built-in cylinder 3, are connected with the same conveying belt 6 through pulley transmission; a motor 8 for driving the third rotating shaft 7 to rotate is arranged at the bottom end of the outer part of the processing box main body 1, the output end of the motor 8 penetrates through the processing box main body 1 and is fixedly connected with one end of the third rotating shaft 7, and a plurality of hollow stirring plates 10 are fixed on the outer parts of the first rotating shaft 4 and the second rotating shaft 5 in a surrounding manner; this structure is that when the processing box body 1 feeds the production raw material of unshaped refractories into the interior of the built-in cylinder 3 through the feed port 2, the motor 8 can drive the third rotating shaft 7 to rotate and drive the conveyor belt 6 to synchronously drive the first rotating shaft 4 and the second rotating shaft 5 to rotate, the first rotating shaft 4 and the second rotating shaft 5 can drive the plurality of stirring plates 10 to rotate to carry out multiple stirring processing on the raw materials when rotating, the grinding roller 11 and the grinding disc 13 can be driven to mutually cooperate to carry out grinding processing on the stirred raw materials when the third rotating shaft 7 rotates, therefore, the processing box body 1 can complete two processes of stirring and grinding the raw materials simultaneously, so that the production process of the unshaped refractory is simplified, the energy consumption is effectively saved, and the trouble that the unshaped refractory needs to be separately completed in different devices during the stirring and grinding processes is avoided.
Two layers of inclined plates 9 which are distributed in a mutually staggered manner are arranged at the upper end and the lower end inside the built-in cylinder 3, the inclined plates 9 are hollow structures and are fixed on the inner wall of the built-in cylinder 3, the two layers of inclined plates 9 are respectively positioned between the first rotating shaft 4 and the second rotating shaft 5 and at intervals between the second rotating shaft 5 and the third rotating shaft 7, and the inclined plates 9 with the structures can slow down the blanking speed of raw materials inside the built-in cylinder 3, so that the uniformity of the raw materials is better in the stirring and grinding processes; a grinding roller 11 is sleeved outside the third rotating shaft 7, and a grinding disc 13 is arranged below the grinding roller 11; both sides of 3 diapalls of built-in section of thick bamboo all are equipped with guide plate 15, and guide plate 15's top surface all is the leanin structure, and this structure guide plate 15 can make the raw materials after accomplishing the processing more smooth and easy carry out the ejection of compact from discharge gate 14, prevents that the raw materials from amassing in the both sides of 3 diapalls of built-in section of thick bamboo.
In the production equipment of the unshaped refractory material, the inner walls of two sides of a feed port 2 are hinged with a baffle 201 in a circular arc structure through a rotating shaft, a groove 202 is formed below the joint of the baffle 201 and the inner wall of the feed port 2, the inside of the groove 202 is connected with a screw rod 203 through a bearing, the outside of the screw rod 203 is sleeved with a threaded sleeve 204 through a threaded structure, a movable rod 205 is connected between the outer side of the threaded sleeve 204 and the bottom of the baffle 201, and two ends of the movable rod 205 are respectively hinged with the outer side of the threaded sleeve 204 and the bottom of the baffle 201; and the outside fixed cover at screw 203 top is equipped with plastics gear 206, and the position that corresponds with plastics gear 206 is equipped with the opening on the bottom wall of recess 202. This structure is when processing case main part 1 adds the raw materials through feed inlet 2, the staff accessible rotates plastic gear 206 and drives screw rod 203 and take place rotatoryly in the inside of recess 202, screw rod 203 can drive thread bush 204 through the helicitic texture when rotatory and reciprocate and make movable rod 205 drive baffle 201 and change inclination, can adjust the pan feeding bore size of feed inlet 2 when baffle 201 folds each other or separates, thereby make feed inlet 2 can carry out accurate control to the input of raw materials, in order to guarantee the production quality to unshaped refractory material.
In the production equipment of the unshaped refractory, four stirring plates 10 are arranged outside the first rotating shaft 4 and the second rotating shaft 5, and the included angles between the stirring plates 10 are 90 degrees, so that the stirring plates 10 can more fully stir raw materials, and the effect of mixing the raw materials is effectively improved; hollow structure's stirring board 10's top is equipped with a plurality of through-hole 1001, and the inside of stirring board 10 is fixed with the separation blade 1002 that a plurality of is equidistant distribution, separation blade 1002 is rectangular form structure, and the outer end of stirring board 10 is open structure, this structure can get into its inside then disperse from between a plurality of separation blade 1002 again through-hole 1001 when the raw materials falls into the top of stirring board 10, this makes stirring board 10 can play the effect of homodisperse to the raw materials stirring in-process, thereby further improve the effect of mixing the raw materials.
In this unshaped refractory's production facility, be equipped with elastic rubber layer 16 between the inner wall of grinding roller 11 and the outer wall of third pivot 7, and elastic rubber layer 16 is the loop configuration, and the inner wall of grinding roller 11 all bonds with elastic rubber layer 16 through adhesive with the outer wall of third pivot 7, and this structure grinding roller 11 can be under elastic rubber layer 16's elastic action force with the top flexible contact who rolls dish 13 to guarantee grinding roller 11 to the effect when rolling the raw materials grinding on the dish 13.
In the production equipment of the unshaped refractory material, the top of the grinding disc 13 is tightly attached to the bottom of the grinding roller 11, a plurality of grinding blocks 12 in semicircular structures are arranged on the top of the grinding disc 13 and the outer part of the grinding roller 11, and the grinding disc 13 and the grinding roller 11 can be in mutual frictional contact through the grinding blocks 12, so that the effect of grinding raw materials is further improved; the border of grinding dish 13 and the inner wall fixed connection of built-in section of thick bamboo 3, and grind the inside of dish 13 and seted up a plurality of hourglass material hole 17 to leak material hole 17 and be located the space department between the grinding piece 12, the raw materials that this structure grinding dish 13 top was accomplished can fall into the bottom of built-in section of thick bamboo 3 through leaking material hole 17.
The working principle is as follows: when the production equipment of the unshaped refractory material is used, firstly, when raw materials are added into the processing box main body 1 through the feeding hole 2 and the input amount needs to be controlled, a worker extends a hand into an opening on the bottom wall of the groove 202 to rotate the plastic gear 206, when the plastic gear 206 drives the screw rod 203 to rotate in the groove 202, the threaded sleeve 204 can move outside the screw rod 203 through a threaded structure, the baffle 201 can be driven by the movable rod 205 to change the inclination angle in the moving process of the threaded sleeve 204, a corresponding feeding caliber can be formed after the baffle 201 is adjusted to a proper inclination angle, at the moment, the raw materials can accurately fall into the inner part of the built-in barrel 3 through the feeding caliber formed by the baffle 201, then the motor 8 is started, the motor 8 drives the third rotating shaft 7 to rotate and the conveyor belt 6 to start transmission, the first rotating shaft 4 and the second rotating shaft 5 are synchronously driven to rotate during transmission of the conveyor belt 6, the first rotating shaft 4 and the second rotating shaft 5 can drive a plurality of stirring plates 10 to rotate to carry out multiple stirring processing on raw materials when rotating, and when the raw materials fall into the top of the stirring plates 10, the raw materials can enter the inside of the stirring plates through the through holes 1001 and then are dispersed among a plurality of blocking pieces 1002, so that the raw materials are dispersed more uniformly, when the raw materials fall onto the top of the inclined plate 9, the inclined plate 9 can play a certain role in slowing down the blanking speed of the raw materials until the raw materials fall onto the rolling disc 13 after being stirred, the third rotating shaft 7 drives the grinding roller 11 and the rolling disc 13 to be in mutual friction contact through rotation, the rolling disc 13 and the grinding roller 11 can be mutually pressed through the rolling block 12 to increase the effect of grinding the raw materials, when the raw materials at the top of the rolling disc 13 are ground, the raw materials fall into the bottom of the built-in barrel 3 through the material leakage hole 17, and finally the guide plate 15 guides the processed raw materials out from the discharge hole 14, thereby completing a series of works.
According to the formula, the high-alumina bauxite is matched with the magnesium aluminate spinel as a main aggregate, so that the overall strength of the refractory material is improved, and the thermal shock resistance and the permeability resistance of the refractory material are further improved by combining the silicon oxide, the zirconium carbide, the semisteel jade and the organic binder, so that the high-temperature volume structure of the material is more compact and stable.
The production equipment of the unshaped refractory material in the preparation method can complete the processes of stirring and grinding the raw materials simultaneously, and simplify the production process of the unshaped refractory material, thereby shortening the production period, reducing the production cost of the process and reducing the energy consumption; the production process is simplified, the energy consumption is saved, meanwhile, various raw materials with different particle sizes can be fully mixed through multi-stage stirring and grinding, and the unshaped refractory material with good thermal shock stability, strong corrosion resistance and strong impermeability is prepared, so that the service life of the furnace lining is prolonged, and the refractory quality of the furnace lining is improved.
The above description is only for the purpose of illustrating the technical solutions of the present invention and not for the purpose of limiting the same, and other modifications or equivalent substitutions made by those skilled in the art to the technical solutions of the present invention should be covered within the scope of the claims of the present invention without departing from the spirit and scope of the technical solutions of the present invention.
Claims (8)
1. The formula of the unshaped refractory material is characterized in that: the aggregate comprises 20-35 parts of high alumina bauxite, 10-30 parts of magnesium aluminate spinel, 10-15 parts of silicon oxide, 5-20 parts of zirconium carbide and 3-8 parts of semisteel; the binding agent comprises 12-26 parts of organic binding agent, wherein the organic binding agent adopts atactic polypropylene or one or more of phenolic resin and absolute ethyl alcohol.
2. The formulation of claim 1, wherein: the magnesium aluminate spinel contains 10-28% of magnesium oxide and 72-90% of aluminum oxide by mass.
3. The formulation of an unshaped refractory according to claim 1, wherein: the preferable mass ratio of the high bauxite to the magnesium aluminate spinel is 1: 1.
4. A method of producing an unshaped refractory according to any one of claims 1 to 3, wherein: the method comprises the following steps:
s1, weighing raw materials: respectively weighing aggregate and a binding agent according to the mass parts, and preparing by adopting production equipment of the unshaped refractory material;
s2, dry mixing, stirring and grinding: the weighed aggregate is placed into a feeding hole (2) at the upper end of a processing box main body (1), and the feeding caliber is adjusted through a movable baffle (201) and a movable rod (205) arranged at the lower end of the feeding hole (2) to control the feeding amount;
aggregate enters a built-in cylinder (3) in a processing box main body (1) after passing through a feeding hole (2), and is subjected to multistage stirring processing through a stirring plate (10) and an inclined plate (9) which are arranged in two layers in the built-in cylinder (3), wherein the stirring time is controlled to be 3-12 min;
the aggregate flows out of a grinding roller (11) after passing through a lower inclined plate (9), grinding and crushing of the aggregate are carried out through a grinding roller (11) and a grinding block (12) correspondingly arranged on a lower-end grinding plate (13), the grinding time is 15-20min, ground aggregate powder falls onto a guide plate (15) at the bottom of a built-in cylinder (3) through a material leakage hole (17) formed in the grinding plate (13), the guide plate (15) collects the aggregate powder and guides the aggregate powder out from a discharge hole (14) at the lower end of a processing box main body (1), and finally dry-mixed aggregate powder is obtained;
s3, forming of mixed binders: putting the obtained dry-mixed aggregate powder and the weighed binding agent into production equipment of the unshaped refractory again for preparation, wherein the mixing and stirring time of the dry-mixed aggregate powder and the binding agent is controlled to be 5-8min, and finally obtaining the unshaped refractory formed by combination after multi-stage stirring;
in the adopted production equipment for the amorphous refractory material, the upper end and the lower end of the processing box main body (1) are respectively provided with the feeding hole (2) and the discharging hole (14), the built-in barrel (3) is arranged inside the processing box main body, and the built-in barrel (3) is internally provided with the first rotating shaft (4), the second rotating shaft (5) and the third rotating shaft (7) from top to bottom in sequence; one ends of the first rotating shaft (4), the second rotating shaft (5) and the third rotating shaft (7) are connected with the inner wall of the built-in cylinder (3) through bearings, the other ends of the first rotating shaft (4), the second rotating shaft (5) and the third rotating shaft (7) are slidably penetrated through the built-in cylinder (3) and are connected with the inner wall of the processing box main body (1) through bearings, and the ends, located outside the built-in cylinder (3), of the first rotating shaft (4), the second rotating shaft (5) and the third rotating shaft (7) are connected with the same conveying belt (6) through pulley transmission;
a motor (8) for driving a third rotating shaft (7) to rotate is arranged at the bottom end of the outer part of the processing box main body (1), and a plurality of stirring plates (10) with hollow structures are fixed on the outer parts of the first rotating shaft (4) and the second rotating shaft (5) in a surrounding manner;
two layers of inclined plates (9) which are distributed in a staggered manner are arranged at the upper end and the lower end of the interior of the built-in barrel (3), the inclined plates (9) are hollow structures and are fixed on the inner wall of the built-in barrel (3), and the two layers of inclined plates (9) are respectively positioned at intervals between the first rotating shaft (4) and the second rotating shaft (5) and between the second rotating shaft (5) and the third rotating shaft (7);
a grinding roller (11) is sleeved outside the third rotating shaft (7), and a grinding disc (13) is arranged below the grinding roller (11); both sides of the bottom wall of the built-in barrel (3) are provided with guide plates (15), and the top surfaces of the guide plates (15) are of inward inclined structures.
5. The method according to claim 4, wherein the method comprises the steps of: in the production equipment of the unshaped refractory, the inner walls of two sides of the feed port (2) are hinged with a baffle (201) in a circular arc structure through a rotating shaft, a groove (202) is formed below the joint of the baffle (201) and the inner wall of the feed port (2), the inside of the groove (202) is connected with a screw rod (203) through a bearing, the outside of the screw rod (203) is sleeved with a threaded sleeve (204) through a threaded structure, a movable rod (205) is connected between the outside of the threaded sleeve (204) and the bottom of the baffle (201), and two ends of the movable rod (205) are hinged with the outside of the threaded sleeve (204) and the bottom of the baffle (201) respectively; and a plastic gear (206) is fixedly sleeved outside the top end of the screw rod (203), and an opening is formed in the bottom wall of the groove (202) and corresponds to the plastic gear (206).
6. The method according to claim 4, wherein the method comprises the steps of: in the production equipment of the unshaped refractory, four stirring plates (10) are arranged outside a first rotating shaft (4) and a second rotating shaft (5), and included angles between the stirring plates (10) are all 90 degrees; the top of hollow structure's stirring board (10) is equipped with a plurality of through-hole (1001), and the inside of stirring board (10) is fixed with separation blade (1002) that a plurality of is equidistant distribution to the outer end of stirring board (10) is open structure.
7. The method according to claim 4, wherein the method comprises the steps of: in the production equipment of the unshaped refractory material, an elastic rubber layer (16) is arranged between the inner wall of the grinding roller (11) and the outer wall of the third rotating shaft (7), and the elastic rubber layer (16) is of an annular structure.
8. The method according to claim 4, wherein the method comprises the steps of: in the production equipment of the unshaped refractory material, the top of the grinding disc (13) is clung to the bottom of the grinding roller (11), and a plurality of grinding blocks (12) with semicircular structures are arranged at the top of the grinding disc (13) and the outer part of the grinding roller (11); the edge of the grinding disc (13) is fixedly connected with the inner wall of the built-in barrel (3), a plurality of material leaking holes (17) are formed in the grinding disc (13), and the material leaking holes (17) are located in gaps between the grinding blocks (12).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210354985.2A CN114671672A (en) | 2022-04-06 | 2022-04-06 | Formula and preparation method of unshaped refractory material |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210354985.2A CN114671672A (en) | 2022-04-06 | 2022-04-06 | Formula and preparation method of unshaped refractory material |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN114671672A true CN114671672A (en) | 2022-06-28 |
Family
ID=82077906
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210354985.2A Pending CN114671672A (en) | 2022-04-06 | 2022-04-06 | Formula and preparation method of unshaped refractory material |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114671672A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117700247A (en) * | 2023-12-18 | 2024-03-15 | 巩义市振华炉料有限公司 | High-strength unshaped refractory material and preparation method thereof |
Citations (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101580403A (en) * | 2009-06-25 | 2009-11-18 | 攀钢冶金材料有限责任公司 | Vanadium extraction converter lining patching material composite and preparation method thereof |
| CN102965497A (en) * | 2012-12-11 | 2013-03-13 | 北京矿冶研究总院 | Feeding and stirring device of hydrometallurgy reactor |
| CN104003743A (en) * | 2014-06-14 | 2014-08-27 | 张婷 | High-alumina brick and manufacturing method thereof |
| CN104030707A (en) * | 2014-06-14 | 2014-09-10 | 张婷 | High-abrasion high-alumina brick with heat shock resistance and manufacturing method thereof |
| CN104150921A (en) * | 2014-07-30 | 2014-11-19 | 长兴攀江冶金材料有限公司 | Aluminum magnesium slag retaining wall |
| CN105108902A (en) * | 2015-07-20 | 2015-12-02 | 章涛 | Concrete mixer |
| CN206008594U (en) * | 2016-08-30 | 2017-03-15 | 浙江安吉天洋滚塑设备有限公司 | The uniform type mixing and stirring tank of high efficiency dispersion |
| CN110451999A (en) * | 2019-08-28 | 2019-11-15 | 云南濮耐昆钢高温材料有限公司 | A kind of aluminum-spinel refractory casting material and preparation method thereof |
| CN211099443U (en) * | 2019-11-12 | 2020-07-28 | 郑州鑫宇飞数码科技有限公司 | Grinding mixer of printing ink |
| CN213194038U (en) * | 2020-08-13 | 2021-05-14 | 浙江凡唯科技有限公司 | Grinding device is used in water based paint production |
| CN214131422U (en) * | 2020-09-30 | 2021-09-07 | 烟台中观生物肥业有限公司 | Raw and other materials preliminary working equipment is used in soil fertilizer production |
| CN113663762A (en) * | 2021-08-12 | 2021-11-19 | 苏州市职业大学 | A raw material mixing and grinding machine |
-
2022
- 2022-04-06 CN CN202210354985.2A patent/CN114671672A/en active Pending
Patent Citations (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101580403A (en) * | 2009-06-25 | 2009-11-18 | 攀钢冶金材料有限责任公司 | Vanadium extraction converter lining patching material composite and preparation method thereof |
| CN102965497A (en) * | 2012-12-11 | 2013-03-13 | 北京矿冶研究总院 | Feeding and stirring device of hydrometallurgy reactor |
| CN104003743A (en) * | 2014-06-14 | 2014-08-27 | 张婷 | High-alumina brick and manufacturing method thereof |
| CN104030707A (en) * | 2014-06-14 | 2014-09-10 | 张婷 | High-abrasion high-alumina brick with heat shock resistance and manufacturing method thereof |
| CN104150921A (en) * | 2014-07-30 | 2014-11-19 | 长兴攀江冶金材料有限公司 | Aluminum magnesium slag retaining wall |
| CN105108902A (en) * | 2015-07-20 | 2015-12-02 | 章涛 | Concrete mixer |
| CN206008594U (en) * | 2016-08-30 | 2017-03-15 | 浙江安吉天洋滚塑设备有限公司 | The uniform type mixing and stirring tank of high efficiency dispersion |
| CN110451999A (en) * | 2019-08-28 | 2019-11-15 | 云南濮耐昆钢高温材料有限公司 | A kind of aluminum-spinel refractory casting material and preparation method thereof |
| CN211099443U (en) * | 2019-11-12 | 2020-07-28 | 郑州鑫宇飞数码科技有限公司 | Grinding mixer of printing ink |
| CN213194038U (en) * | 2020-08-13 | 2021-05-14 | 浙江凡唯科技有限公司 | Grinding device is used in water based paint production |
| CN214131422U (en) * | 2020-09-30 | 2021-09-07 | 烟台中观生物肥业有限公司 | Raw and other materials preliminary working equipment is used in soil fertilizer production |
| CN113663762A (en) * | 2021-08-12 | 2021-11-19 | 苏州市职业大学 | A raw material mixing and grinding machine |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117700247A (en) * | 2023-12-18 | 2024-03-15 | 巩义市振华炉料有限公司 | High-strength unshaped refractory material and preparation method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN207680500U (en) | A kind of simple mixing device | |
| CN106626007A (en) | Building material molding device capable of achieving automatic discharging | |
| CN114471848B (en) | A high-fineness ball milling equipment for quartz ceramic processing | |
| CN107309029A (en) | A kind of mixed grind device for producing refractory material | |
| CN205109763U (en) | Energy -conserving ceramic tile production ball -milling slurrying device | |
| CN207415705U (en) | A kind of concrete mixing plant powder feed arrangement | |
| CN111086109A (en) | Ceramic machining is with multi-functional quantitative blendor | |
| CN116924715B (en) | Green low-carbon high-performance admixture and manufacturing process and manufacturing equipment thereof | |
| CN210875166U (en) | A mix machine that is used for converter dust removal to press ball production | |
| CN207357258U (en) | A kind of mixed grind device for producing refractory material | |
| CN118990799A (en) | Processing device for producing cement solid waste cementing material | |
| CN222900908U (en) | Corundum brick raw material mixing device | |
| CN111829337B (en) | High temperature alumina calcination apparatus | |
| CN116041076B (en) | Production process and application of high-wear-resistance silicon mullite brick | |
| CN212092663U (en) | A grinding device for refractory processing | |
| CN222012676U (en) | A rotary kiln for preparing white cement fuel | |
| CN207591974U (en) | Ceramic material ball mill | |
| CN110314579A (en) | The operating method of assembly line graphite stirring facility | |
| CN208627503U (en) | A kind of grinding device for ceramic tile production process | |
| CN212457958U (en) | Discharging device for cement clinker grate type cooler | |
| CN118237140B (en) | A method for preparing polylight mullite microporous homogenized material | |
| CN217093792U (en) | Modifying device for rotary kiln mill | |
| CN209775082U (en) | A vacuum furnace refining high-performance air-permeable brick production system | |
| CN112010576A (en) | Cement clinker processing technology | |
| CN222387265U (en) | Raw material stirring equipment for brickmaking |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20220628 |
|
| RJ01 | Rejection of invention patent application after publication |