CN114536767A - Modular jumbo size polymer 3D prints aftertreatment device - Google Patents
Modular jumbo size polymer 3D prints aftertreatment device Download PDFInfo
- Publication number
- CN114536767A CN114536767A CN202210337477.3A CN202210337477A CN114536767A CN 114536767 A CN114536767 A CN 114536767A CN 202210337477 A CN202210337477 A CN 202210337477A CN 114536767 A CN114536767 A CN 114536767A
- Authority
- CN
- China
- Prior art keywords
- plate
- processing device
- printing
- size polymer
- polymer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C64/00—Additive manufacturing, i.e. manufacturing of three-dimensional [3D] objects by additive deposition, additive agglomeration or additive layering, e.g. by 3D printing, stereolithography or selective laser sintering
- B29C64/30—Auxiliary operations or equipment
- B29C64/379—Handling of additively manufactured objects, e.g. using robots
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C35/00—Heating, cooling or curing, e.g. crosslinking or vulcanising; Apparatus therefor
- B29C35/02—Heating or curing, e.g. crosslinking or vulcanizing during moulding, e.g. in a mould
- B29C35/04—Heating or curing, e.g. crosslinking or vulcanizing during moulding, e.g. in a mould using liquids, gas or steam
- B29C35/045—Heating or curing, e.g. crosslinking or vulcanizing during moulding, e.g. in a mould using liquids, gas or steam using gas or flames
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B33—ADDITIVE MANUFACTURING TECHNOLOGY
- B33Y—ADDITIVE MANUFACTURING, i.e. MANUFACTURING OF THREE-DIMENSIONAL [3D] OBJECTS BY ADDITIVE DEPOSITION, ADDITIVE AGGLOMERATION OR ADDITIVE LAYERING, e.g. BY 3D PRINTING, STEREOLITHOGRAPHY OR SELECTIVE LASER SINTERING
- B33Y40/00—Auxiliary operations or equipment, e.g. for material handling
- B33Y40/20—Post-treatment, e.g. curing, coating or polishing
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Manufacturing & Machinery (AREA)
- Materials Engineering (AREA)
- Physics & Mathematics (AREA)
- Health & Medical Sciences (AREA)
- Oral & Maxillofacial Surgery (AREA)
- Thermal Sciences (AREA)
- Robotics (AREA)
- Mechanical Engineering (AREA)
- Optics & Photonics (AREA)
Abstract
本发明提供的一种组合式大尺寸聚合物3D打印后处理装置,包括若干个加热板,若干个加热板拼接连接形成组合式的框型结构,所述框型结构的底部为开口端;本发明能实现大尺寸聚合物打印完成后的即时热处理,降低大尺寸聚合物打印件的变形,打印件后处理时,该组合后处理装置与打印件是互不约束的,可使打印件残余应力自由释放,不会收到外在的挤压变形。
A combined large-size polymer 3D printing post-processing device provided by the present invention includes several heating plates, and the several heating plates are spliced and connected to form a combined frame-shaped structure, and the bottom of the frame-shaped structure is an open end; The invention can realize the instant heat treatment after the printing of the large-sized polymer, and reduce the deformation of the large-sized polymer printing. Freely released, will not receive external squeezing deformation.
Description
技术领域technical field
本发明属于3D打印领域,具体涉及一种组合式大尺寸聚合物3D打印后处理装置。The invention belongs to the field of 3D printing, in particular to a combined large-size polymer 3D printing post-processing device.
背景技术Background technique
融沉积成型(Fused deposition modeling,FDM)是一种广泛应用的聚合物3D打印成型技术。在这一增材制造技术中,塑料聚合物被加热熔化以熔体的形式堆积粘附在预定的打印位置,打印制品最终由熔体逐条逐层堆积粘结成型。Fused deposition modeling (FDM) is a widely used polymer 3D printing technology. In this additive manufacturing technology, the plastic polymer is heated and melted in the form of a melt and adhered to a predetermined printing position, and the printed product is finally formed by the melt layer by layer.
在这个过程中,当前打印层的熔融聚合物在下层聚合物的上表面冷却和凝固时,会出现收缩现象,但由于受到下方已硬化结构的限制,这种收缩会导致层与层之间形成剪切力,即残余应力,这种残余应力一层一层累计起来具有极大的破坏性,可能导致零件变形,使其边缘卷起,甚至脱离支撑。During this process, as the molten polymer of the front print layer cools and solidifies on the upper surface of the underlying polymer, shrinkage occurs, but due to the constraints of the hardened structure below, this shrinkage can cause layer-to-layer formation Shear force, or residual stress, can be extremely destructive layer by layer and can cause parts to deform, roll up their edges, or even break away from supports.
一般通过机械固定或化学粘接的方法来提高打印件与底板的结合效果来抑制打印件由于边缘卷起而导致的脱离底板,但当打印件被取下后,由于残余应力并未释放完全,在无约束的条件下仍会缓慢地进行释放,导致打印件变形,变形严重的甚至导致打印件报废。Generally, the bonding effect between the printed part and the base plate is improved by mechanical fixing or chemical bonding to suppress the printed part from being separated from the base plate due to the edge rolling. However, when the printed part is removed, the residual stress is not completely released. Under unconstrained conditions, it will still be released slowly, resulting in the deformation of the printed part, and even the printed part will be scrapped if the deformation is serious.
制件尺寸越大残余应力越大,一般的处理方法是打印完成之后,去除约束将其在一定温度下进行热处理,但在无约束状态下的后处理过程打印件仍会产生部分变形,导致打印件尺寸偏差较大。The larger the size of the part, the greater the residual stress. The general treatment method is to remove the constraint and heat treatment at a certain temperature after the printing is completed. However, the printed part will still be partially deformed during the post-processing process in the unconstrained state, resulting in printing. Piece size deviation is large.
现有技术中,对打印件后处理时采用的方法有:In the prior art, the methods used in post-processing the prints are:
1、现有关于聚合物3D打印的处理方法多数集中于如何提高表面质量,因为大多聚合物打印尺寸较小(最大尺寸1m以内),这些小尺寸打印件在抑制变形方面比较容易实现,残余应力较小,通过打印前留余量,后期机械加工的方式可以达到要求的表面尺寸及精度;1. Most of the existing processing methods for polymer 3D printing focus on how to improve the surface quality, because most of the polymer printing size is small (within the maximum size of 1m), these small-size printing parts are easier to achieve in terms of suppressing deformation, residual stress Small, by leaving a margin before printing, the required surface size and accuracy can be achieved by machining in the later stage;
2、《一种基于FDM技术的3D打印后处理工艺》中介绍的聚合物3D打印后处理方法就是通过预留加工余量来弥补变形,同时增加打印过程中打印件与基板的结合力来抑制变形,打印完成后直接机械加工的方法来达到要求的尺寸及表面精度,事实上,当制件尺寸比较大(1m尺寸以上)且结构比较容易变形的打印件,往往无法通过预留加工余量的方法来弥补变形;2. The post-processing method of polymer 3D printing introduced in "A Post-processing Process of 3D Printing Based on FDM Technology" is to make up for the deformation by reserving machining allowance, and at the same time increase the bonding force between the printed part and the substrate during the printing process to inhibit Deformation, the method of direct machining after printing is completed to achieve the required size and surface accuracy. In fact, when the size of the workpiece is relatively large (above 1m size) and the structure is relatively easy to deform, it is often impossible to reserve machining allowances. method to compensate for the deformation;
3、现有技术也有通过热处理的方法来减少残余应力,但一般都是将制件取下,或与基板一起放入加热容器种进行后处理,但当制件较大,取下不方便(一般基板是固定死的),且取下后在无约束状态下后处理,仍会在残余应力作用下发生变形,导致尺寸精度变差。3. In the prior art, there is also a method of reducing residual stress by heat treatment, but generally the workpiece is removed, or placed in a heating container together with the substrate for post-processing, but when the workpiece is large, it is inconvenient to remove ( Generally, the substrate is fixed), and after it is removed and post-processed in an unconstrained state, it will still deform under the action of residual stress, resulting in poor dimensional accuracy.
发明内容SUMMARY OF THE INVENTION
本发明的目的在于提供一种组合式大尺寸聚合物3D打印后处理装置,解决了现有技术中存在的上述不足。The purpose of the present invention is to provide a combined large-size polymer 3D printing post-processing device, which solves the above-mentioned deficiencies in the prior art.
为了达到上述目的,本发明采用的技术方案是:In order to achieve the above object, the technical scheme adopted in the present invention is:
本发明提供的一种组合式大尺寸聚合物3D打印后处理装置,包括若干个加热板,若干个加热板拼接连接形成组合式的框型结构,所述框型结构的底部为开口端;且两个相邻的加热板之间可拆卸式连接。A combined large-size polymer 3D printing post-processing device provided by the present invention includes a plurality of heating plates, and the plurality of heating plates are spliced and connected to form a combined frame-shaped structure, and the bottom of the frame-shaped structure is an open end; and Removable connection between two adjacent heating plates.
优选地,两个相邻的加热板之间通过搭扣连接。Preferably, two adjacent heating plates are connected by snaps.
优选地,两个相邻的加热板之间卡接连接。Preferably, two adjacent heating plates are connected by snap connection.
优选地,所述加热板包括外板,所述外板的一端面开设有卡槽,所述卡槽内从内至外依次设置有保温板和加热圈,所述加热圈朝向框型结构内腔一侧。Preferably, the heating plate includes an outer plate, and one end surface of the outer plate is provided with a card slot, and a heat preservation plate and a heating ring are sequentially arranged in the card slot from the inside to the outside, and the heating ring faces the inside of the frame structure. side of the cavity.
优选地,所述外板上还安装有风扇,所述风扇置于保温板和加热圈之间,且风扇的风向朝向加热圈一侧。Preferably, a fan is also installed on the outer plate, the fan is placed between the thermal insulation board and the heating ring, and the wind direction of the fan is toward one side of the heating ring.
优选地,所述外板上还安装有匀风板,所述均风板置于加热圈的外侧。Preferably, an air distribution plate is also installed on the outer plate, and the air distribution plate is placed on the outer side of the heating ring.
优选地,所述均风板上安装有用于测量内腔温度的温控探头。Preferably, a temperature control probe for measuring the temperature of the inner cavity is installed on the air equalizing plate.
优选地,所述框型结构的底部设置有支座。Preferably, the bottom of the frame-shaped structure is provided with a support.
优选地,所述框型结构的底部设置有万向轮。Preferably, the bottom of the frame-shaped structure is provided with a universal wheel.
与现有技术相比,本发明的有益效果是:Compared with the prior art, the beneficial effects of the present invention are:
本发明提供的一种组合式大尺寸聚合物3D打印后处理装置,采用可组合式的加热板,对打印完成的工件进行后处理,工件不需要移动,不需要脱约束,最大限度减少应力变形;且组装、搬运方便,能实现大尺寸聚合物打印完成后的即时热处理,降低大尺寸聚合物打印件的变形,打印件后处理时,该组合后处理装置与打印件是互不约束的,可使打印件残余应力自由释放,不会收到外在的挤压变形。The invention provides a combined large-size polymer 3D printing post-processing device, which adopts a combinable heating plate to post-process the printed workpiece, the workpiece does not need to be moved, and does not need to be unconstrained, and the stress deformation is minimized. ; And it is easy to assemble and transport, and it can realize the instant heat treatment after the printing of the large-size polymer, reduce the deformation of the large-size polymer print. The residual stress of the printed part can be released freely without external extrusion deformation.
附图说明Description of drawings
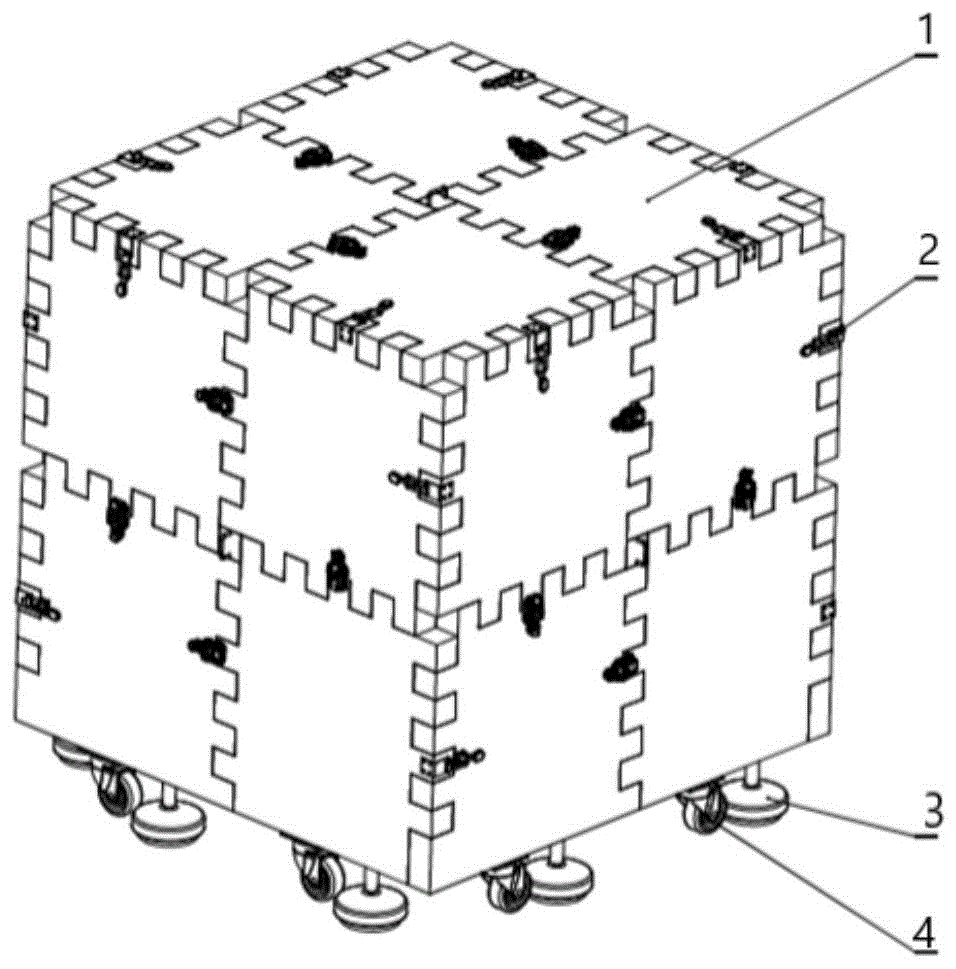
图1是后处理装置的整体结构示意图;Fig. 1 is the overall structure schematic diagram of post-processing device;
图2是加热板结构示意图;Fig. 2 is a schematic diagram of a heating plate structure;
其中,1、加热板 2、搭扣 3、支座 4、万向轮 1、外板 2、保温板 3、风扇安装板 4、风扇 5、加热圈 6、匀风板 7、温控探头。Among them, 1,
具体实施方式Detailed ways
下面结合附图,对本发明进一步详细说明。The present invention will be described in further detail below with reference to the accompanying drawings.
如图1和图2所示,本发明提供的一种组合式大尺寸聚合物3D打印后处理装置,包括若干个加热板1,若干个加热板1拼接连接形成组合式的立方体结构;同时,两个相邻的加热板1之间通过搭扣2活动连接。As shown in FIG. 1 and FIG. 2 , a combined large-size polymer 3D printing post-processing device provided by the present invention includes
所述置于立方体结构的下端面均布有多个支座3和万向轮4。立方体下端安装万向轮4,可将立方体下端拼接块移至任意位置。待位置固定后放下支座3将立方体下端固定在指定位置,而后拼接立方体上端部分。A plurality of
所述加热板1包括外板11、保温板12、风扇安装板13、风扇14、加热圈15、匀风板16和温控探头17,其中,所述外板11为方形板状结构,方形板状结构的四边为锯齿状结构;用于实现相邻的两个外板11之间的卡接连接。The
所述外板11的一端面开设有卡槽,所述卡槽内从内至外依次设置有保温板12、风扇安装板13、加热圈15和匀风板16。One end surface of the
所述风扇安装板13上开设有多个安装孔,所述安装孔内配合安装有风扇14。The
所述均风板16包括板体,所述板体上开设有多个出风口。The
多个出风口自中心向径向发散布置,且从中心向外围孔径依次变大。A plurality of air outlets are arranged radially from the center, and the apertures increase sequentially from the center to the periphery.
每层出风口同轴布置。The air outlets on each floor are arranged coaxially.
所述均风板16上安装有用于测量框型结构内腔中温度的温控探头17。A
所述温控探头17的输出端连接有控制器,所述控制器的输出端与加热圈15控制连接。The output end of the
在使用时,When in use,
将3D打印件打印完成后保持原位置不动,根据打印件尺寸大小选择不同数量的拼接块,每个拼接块通过锁扣连接;例如,打印件尺寸为1300*1300*1300mm时,由于每个拼接块尺寸为500*500*500mm,需选择45个拼接块,组成1500*1500*1500mm的底部开放的立方体将打印件包围其中进行退火处理。After the 3D print is printed, keep the original position unchanged, select different numbers of splicing blocks according to the size of the print, and each splicing block is connected by a lock; for example, when the print size is 1300*1300*1300mm, because each The size of the splicing block is 500*500*500mm, and 45 splicing blocks need to be selected to form a 1500*1500*1500mm cube with an open bottom to surround the printed part for annealing treatment.
本发明对打印件进行后处理时,高分子材料成型后,在合适的温度下进行退火处理,可使链段发生运动,从而使得分子链逐渐由蜷曲状态转变为自然舒展状态,最终达到消除内应力的效果。When the present invention performs post-processing on the printed part, after the polymer material is formed, annealing treatment is performed at a suitable temperature, so that the chain segments can move, so that the molecular chain gradually changes from a curled state to a natural stretched state, and finally achieves elimination of internal effect of stress.
本发明涉及的结构具有以下优点:The structure involved in the present invention has the following advantages:
1、采用可组合式的加热板,对打印完成的工件进行后处理,工件不需要移动,不需要脱约束,最大限度减少应力变形;且组装、搬运方便,能实现大尺寸聚合物打印完成后的即时热处理,降低大尺寸聚合物打印件的变形。1. A composable heating plate is used to post-process the printed workpiece. The workpiece does not need to be moved or unconstrained, and the stress and deformation are minimized; and the assembly and handling are convenient, which can realize the large-scale polymer printing after the completion of the printing. Instant heat treatment to reduce distortion in large-sized polymer prints.
2、打印件后处理时,该组合后处理装置与打印件是互不约束的,可使打印件残余应力自由释放,不会收到外在的挤压变形。2. During the post-processing of the printed parts, the combined post-processing device and the printed parts are not constrained by each other, so that the residual stress of the printed parts can be released freely without external extrusion deformation.
3、加热板分不同规格,可以根据打印件尺寸大小自由组合最佳尺寸,减少加热空间浪费,提高热量利用率,降低不必要的热量损耗。3. The heating plate is divided into different specifications, and the optimal size can be freely combined according to the size of the print, reducing the waste of heating space, improving the utilization rate of heat, and reducing unnecessary heat loss.
4、加热板内外板之间有鼓风装置,内板表面有点阵结构,以保证打印工件周边区域温度分布更为均匀。4. There is a blower device between the inner and outer plates of the heating plate, and the surface of the inner plate has a lattice structure to ensure a more uniform temperature distribution in the surrounding area of the printed workpiece.
5、加热板底部装有滚轮,便于加热板的转移搬运。5. The bottom of the heating plate is equipped with rollers, which is convenient for the transfer and handling of the heating plate.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210337477.3A CN114536767A (en) | 2022-03-31 | 2022-03-31 | Modular jumbo size polymer 3D prints aftertreatment device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210337477.3A CN114536767A (en) | 2022-03-31 | 2022-03-31 | Modular jumbo size polymer 3D prints aftertreatment device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN114536767A true CN114536767A (en) | 2022-05-27 |
Family
ID=81665904
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210337477.3A Pending CN114536767A (en) | 2022-03-31 | 2022-03-31 | Modular jumbo size polymer 3D prints aftertreatment device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114536767A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117227146A (en) * | 2023-09-21 | 2023-12-15 | 广西电网有限责任公司南宁供电局 | A device for making a moldable tool placing plate |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN205980693U (en) * | 2016-07-12 | 2017-02-22 | 广州市浩燃机电设备有限公司 | Device is burned with waste gas to direct combustion heating of synthetic leather |
| CN109676921A (en) * | 2019-02-17 | 2019-04-26 | 乐清市智能装备与制造研究院 | A kind of molding space self-adaptation three-dimensional printing equipment |
| CN110481013A (en) * | 2019-09-27 | 2019-11-22 | 西安增材制造国家研究院有限公司 | A kind of easy pickup polymer three-dimensional printing bottom plate of large scale warpage preventing and Method of printing |
| CN212445697U (en) * | 2020-07-28 | 2021-02-02 | 江西广迪智能钢艺集团有限公司 | Stand concatenation piece mould |
| CN217144929U (en) * | 2022-03-31 | 2022-08-09 | 西安增材制造国家研究院有限公司 | Combined type large-size polymer 3D printing post-processing device |
-
2022
- 2022-03-31 CN CN202210337477.3A patent/CN114536767A/en active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN205980693U (en) * | 2016-07-12 | 2017-02-22 | 广州市浩燃机电设备有限公司 | Device is burned with waste gas to direct combustion heating of synthetic leather |
| CN109676921A (en) * | 2019-02-17 | 2019-04-26 | 乐清市智能装备与制造研究院 | A kind of molding space self-adaptation three-dimensional printing equipment |
| CN110481013A (en) * | 2019-09-27 | 2019-11-22 | 西安增材制造国家研究院有限公司 | A kind of easy pickup polymer three-dimensional printing bottom plate of large scale warpage preventing and Method of printing |
| CN212445697U (en) * | 2020-07-28 | 2021-02-02 | 江西广迪智能钢艺集团有限公司 | Stand concatenation piece mould |
| CN217144929U (en) * | 2022-03-31 | 2022-08-09 | 西安增材制造国家研究院有限公司 | Combined type large-size polymer 3D printing post-processing device |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117227146A (en) * | 2023-09-21 | 2023-12-15 | 广西电网有限责任公司南宁供电局 | A device for making a moldable tool placing plate |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP4789039B2 (en) | Nanoimprint equipment | |
| CN101185966B (en) | Large-scale steel casting production technology and slowly cooling device thereof | |
| JP5077764B2 (en) | Imprint method and apparatus | |
| CN105598448B (en) | A kind of control method of metal material laser 3D printing preheating temperature in situ | |
| CN101526641A (en) | Production line of light guide plate | |
| CN1966436B (en) | Glass substrate and a manufacturing method thereof | |
| CN116118056A (en) | Composite material air inlet channel product forming tool based on memory core die | |
| CN217144929U (en) | Combined type large-size polymer 3D printing post-processing device | |
| CN106673410A (en) | Cooling device and cooling method for 3D (three-dimensional) curved glass hot-pressing equipment | |
| CN202922954U (en) | Adhesive film preparation device capable of improving shrinkage ratio of EVA (Ethylene-Vinyl Acetate) adhesive film | |
| JP5560820B2 (en) | Manufacturing method of fine shape transfer sheet | |
| CN116766522A (en) | Quantitative injection mold for rapidly cooling mobile phone shell and application method of quantitative injection mold | |
| JP3231393U (en) | Light guide film halftone dot processing equipment | |
| CN211970058U (en) | Turnover tray for optimizing precision optical product process | |
| CN221971622U (en) | Double-deck ageing oven device | |
| JP2004337913A (en) | Fine pattern press molding method | |
| JP2013112592A (en) | Apparatus and method for molding optical element | |
| CN205463620U (en) | Add fever type battery pole piece rolling machine | |
| CN205614813U (en) | Foaming cement board core forming die and forming device | |
| CN222007605U (en) | Annealing and heating device for glass wine bottle | |
| CN217704652U (en) | Online automatic adjustment warping system in light guide plate manufacturing process | |
| CN219028669U (en) | Mould preheating device | |
| CN204919118U (en) | Washing machine observation window tray | |
| CN109037139B (en) | carrier | |
| CN211492100U (en) | A molding die for the preparation of concrete blocks |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination |