CN114310065A - Heat exchanger welding bead rapid cooling device - Google Patents
Heat exchanger welding bead rapid cooling device Download PDFInfo
- Publication number
- CN114310065A CN114310065A CN202210128859.5A CN202210128859A CN114310065A CN 114310065 A CN114310065 A CN 114310065A CN 202210128859 A CN202210128859 A CN 202210128859A CN 114310065 A CN114310065 A CN 114310065A
- Authority
- CN
- China
- Prior art keywords
- heat exchanger
- locating plate
- frame
- bead
- welding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000003466 welding Methods 0.000 title claims abstract description 76
- 239000011324 bead Substances 0.000 title claims abstract description 29
- 238000001816 cooling Methods 0.000 title claims abstract description 10
- 238000010791 quenching Methods 0.000 claims 9
- 230000000171 quenching effect Effects 0.000 claims 9
- 230000000149 penetrating effect Effects 0.000 abstract description 5
- 238000000034 method Methods 0.000 description 4
- 238000009792 diffusion process Methods 0.000 description 3
- 239000002184 metal Substances 0.000 description 2
- 230000004075 alteration Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 239000012535 impurity Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
Images



Landscapes
- Heat Treatment Of Articles (AREA)
- Heat-Exchange Devices With Radiators And Conduit Assemblies (AREA)
Abstract
The invention discloses a rapid cooling device for a welding bead of a heat exchanger, which comprises a frame, a positioning plate and an air guide pipe, wherein the positioning plate is slidably arranged on the inner side of the frame, the center of the surface of the positioning plate is provided with a positioning groove in a penetrating manner, hollow cavities are respectively arranged in the two ends of the positioning plate, the two ends of the lower surface of the positioning plate are uniformly provided with exhaust holes penetrating through the hollow cavities, the air guide pipe penetrating through the hollow cavities is fixedly arranged on one side of the positioning plate, and a control valve is fixedly arranged on one side, close to the positioning plate, of the air guide pipe; according to the invention, the frame is arranged above the position to be welded of the heat exchanger, the position to be welded is positioned under the center line of the frame, the welding gun head is fixed in the positioning groove, and the positioning plate is slid in the frame, so that the welding gun head is pushed to move linearly in the frame, and meanwhile, the welding gun head is welded linearly at the position to be welded on the heat exchanger, the welding trend is convenient to control, and the welding efficiency is improved.
Description
Technical Field
The invention relates to the technical field of cooling, in particular to a rapid cooling device for a welding bead of a heat exchanger.
Background
When the heat exchanger is assembled, metal components need to be welded and assembled together, and then a welding bead is formed at the welding position; the weld bead is a single weld formed by each deposition when metal is welded.
However, under the conditions of the existing welding technology, when a weld bead is welded manually, the trend of the weld bead is not easy to control, the welding efficiency is reduced, and the surface precision of a welded part is poor due to a large heat affected zone, so that the welding quality is reduced.
Disclosure of Invention
The invention aims to provide a rapid cooling device for a welding bead of a heat exchanger, which aims to solve the problems that when the welding bead is manually welded, the trend of the welding bead is not easy to control, the welding efficiency is reduced, the surface precision of a welded part is poor due to a large heat affected zone, and the welding quality is reduced.
In order to achieve the purpose, the invention provides the following technical scheme: heat exchanger welding bead rapid cooling device, including frame, locating plate and air duct, the inboard slidable mounting of frame has the locating plate, the center department on locating plate surface runs through and has seted up the constant head tank, well cavity has all been seted up to the inside at locating plate both ends, the both ends of locating plate lower surface have evenly been seted up and have been run through the exhaust hole of well cavity, locating plate one side fixed mounting has runs through the air duct of well cavity, be close to on the air duct one side fixed mounting of locating plate has control flap.
The frame is characterized in that first sliding rods are symmetrically and fixedly mounted on the inner side of the frame, first sliding sleeves matched with the first sliding rods are fixedly mounted on two sides of the positioning plate, and the positioning plate is slidably mounted on the inner side of the frame through the matching of the first sliding sleeves and the first sliding rods.
Wherein, the base is installed to four equal screw threads in edge of frame lower surface.
Wherein, the inside symmetrical slidable mounting of constant head tank has the grip block.
The clamping plate is characterized in that a second sliding rod is fixedly mounted at two ends inside the positioning groove, a second sliding sleeve matched with the second sliding rod is fixedly mounted at two ends of the clamping plate, and the clamping plate is slidably mounted inside the positioning groove in a matched manner through the second sliding sleeve and the second sliding rod.
Wherein, the locating plate surface is located the both sides of constant head tank are all run through and have been seted up the movable groove, the inside threaded mounting of movable groove runs through the screw lead screw of constant head tank, the screw lead screw is located the inside one end of constant head tank with the grip block rotates to be connected.
And a turntable is fixedly arranged at one end of the threaded screw rod, which is positioned in the movable groove.
The thread screw rod is located one end inside the positioning groove and is provided with a smooth end, a shaft sleeve matched with the smooth end is fixedly installed at the center of the back face of the clamping plate, and the thread screw rod is matched with the shaft sleeve through the smooth end and is rotatably connected with the clamping plate.
Wherein, the hollow cavity is arranged perpendicular to the first slide bar.
The positioning plate comprises a positioning plate and a hollow cavity, wherein the hollow cavity is arranged in two, the two hollow cavities are arranged in parallel, one hollow cavity is arranged inside the front end of the positioning plate, and the other hollow cavity is arranged inside the rear end of the positioning plate.
Compared with the prior art, the invention has the beneficial effects that:
the frame is arranged above the position to be welded of the heat exchanger, the position to be welded is located right below the center line of the frame, the welding gun head is fixed in the positioning groove, the positioning plate slides in the frame, the welding gun head is pushed to move linearly in the frame, and meanwhile the welding gun head performs linear welding on the position to be welded on the heat exchanger, so that the welding trend is convenient to control, and the welding efficiency is improved;
when the welding device is used for welding, the air blower externally connected with the air guide pipe is opened, wind power generated by the air blower is conveyed into the hollow cavity through the air guide pipe, then the wind power is blown out through the exhaust hole and is blown to the welding position, so that the temperature of a welded welding bead is reduced, the diffusion of heat generated during welding is reduced, the area of heat expansion is reduced, the surface precision of a welded part is improved, and the welding quality is improved.
Drawings
FIG. 1 is a schematic top view of the present invention;
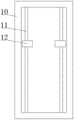
FIG. 2 is a schematic top view of the frame of the present invention;
FIG. 3 is a schematic top view of a positioning plate according to the present invention;
FIG. 4 is a schematic bottom view of the present invention;
FIG. 5 is a schematic bottom view of the positioning plate of the present invention;
FIG. 6 is a schematic side view of the present invention.
In FIGS. 1-6: 10. a frame; 11. a first slide bar; 12. a first sliding sleeve; 13. a base; 20. positioning a plate; 21. positioning a groove; 22. a movable groove; 23. a hollow cavity; 24. an exhaust hole; 25. a threaded lead screw; 26. a turntable; 27. a second slide bar; 30. an air duct; 31. a control valve; 40. a clamping plate; 41. and the second sliding sleeve.
Detailed Description
The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only a part of the embodiments of the present invention, and not all of the embodiments. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
Referring to fig. 1-6, the present invention provides a technical solution: heat exchanger welding bead rapid cooling device, including frame 10, locating plate 20 and air duct 30, frame 10 inboard slidable mounting has locating plate 20, the central department on locating plate 20 surface runs through and has seted up constant head tank 21, well cavity 23 has all been seted up to the inside at locating plate 20 both ends, the both ends of locating plate 20 lower surface are evenly seted up and are run through the exhaust hole 24 of cavity 23 in, locating plate 20 one side fixed mounting has the air duct 30 that runs through well cavity 23, one side fixed mounting that is close to locating plate 20 on the air duct 30 has control flap 31.
The frame 10 is arranged above the position to be welded of the heat exchanger, the position to be welded is located under the center line of the frame 10, the welding gun head is fixed in the positioning groove 21, the positioning plate 20 slides in the frame 10, the welding gun head is pushed to move linearly in the frame 10, meanwhile, the position to be welded of the welding gun head on the heat exchanger is welded linearly, the welding trend is convenient to control, and the welding efficiency is improved.
Wherein, the tip and the external air-blower fixed connection of air duct 30, produce wind-force through the air-blower, then carry the wind-force that the air-blower produced for well cavity 23 through air duct 30, when welding, open the external air-blower of air duct 30, then carry the wind-force that the air-blower produced through air duct 30 in well cavity 23, then blow off wind-force through exhaust hole 24, and blow wind-force on the welding position, thereby cool down the welding bead after the welding and handle, reduce the diffusion of the heat that produces during the welding, the region that the heat enlarges has been reduced, the precision on welding part surface has been improved, and the welding quality is improved.
Wherein, the inboard symmetry fixed mounting of frame 10 has first slide bar 11, the equal fixed mounting in locating plate 20 both sides has the first sliding sleeve 12 of the first slide bar 11 of cooperation, locating plate 20 is through first sliding sleeve 12 and the cooperation slidable mounting of first slide bar 11 in frame 10 inboard, through first sliding sleeve 12 and the cooperation of first slide bar 11, made things convenient for at the inside sliding positioning plate 20 of frame 10, when carrying out welding process to the heat exchanger, can promote locating plate 20 along first slide bar 11 and remove, thereby carry out the linear welding on the heat exchanger, be convenient for control the welding trend.
Wherein, the base 13 is installed to the equal screw thread in four edges of frame 10 lower surface, when treating the position of welding with frame 10 setting at the heat exchanger, can adjust the height of frame 10 through base 13, can bond base 13 on the heat exchanger simultaneously to fix frame 10 on the heat exchanger through base 13, prevent at the welded in-process, frame 10 takes place the skew.
The clamping plates 40 are symmetrically and slidably mounted inside the positioning groove 21, the movable grooves 22 are formed in the surface of the positioning plate 20 in a penetrating mode on two sides of the positioning groove 21, the threaded screw rod 25 penetrating through the positioning groove 21 is mounted in the movable grooves 22 in a threaded mode, and one end, located inside the positioning groove 21, of the threaded screw rod 25 is rotatably connected with the clamping plates 40; a rotary table 26 is fixedly arranged at one end of the threaded screw rod 25 positioned in the movable groove 22; the one end that screw rod 25 is located the inside of constant head tank 21 is provided with smooth end, and the center department fixed mounting at the backplate 40 back has the axle sleeve of the smooth end of cooperation, and screw rod 25 is connected with the rotation of grip block 40 through smooth end and axle sleeve cooperation.
Before welding the heat exchanger, fixing the frame 10 on a position to be welded of the heat exchanger, setting the welding gun head between the two clamping plates 40, rotating the threaded screw rod 25 through the turntable 26, pushing the clamping plates 40 to move inwards through the threaded screw rod 25, reducing the distance between the two clamping plates 40, and fixing the welding gun head in the positioning groove 21 through the two clamping plates 40.
Wherein, the inside both ends of constant head tank 21 all fixed mounting have the second slide bar 27, the equal fixed mounting in grip block 40 both ends has the second sliding sleeve 41 of cooperation second slide bar 27, grip block 40 passes through second sliding sleeve 41 and second slide bar 27 cooperation slidable mounting inside constant head tank 21, through the cooperation of second sliding sleeve 41 and second slide bar 27, made things convenient for the position at constant head tank 21 inside regulation grip block 40, and can restrict the position of backup pad 40, prevent that backup pad 40 from rotating along with screw lead screw 25.
Wherein, well cavity 23 sets up with first slide bar 11 is perpendicular, well cavity 23 is provided with two, two well cavity 23 parallel arrangement, well cavity 23 sets up the inside at locating plate 20 front end, another well cavity 23 sets up the inside at locating plate 20 rear end, when welding the heat exchanger like this, can form a decurrent wind-force behind the front end of welding position and rear end, wind-force in welding bead the place ahead can blow away the dust of treating the welding position, avoid the welding department to have impurity, the wind-force in welding bead rear can be handled the welding bead cooling.
The working principle is as follows: when the welding gun is used, the frame 10 is fixed at a position to be welded of the heat exchanger, then a welding gun head is arranged between the two clamping plates 40, the threaded screw rod 25 is rotated through the rotary disc 26, the clamping plates 40 are pushed to move inwards through the threaded screw rod 25, so that the distance between the two clamping plates 40 is reduced, then the welding gun head is fixed in the positioning groove 21 through the two clamping plates 40, the position of the welding gun head is right above a welding seam, then the positioning plate 20 is conveniently slid in the frame 10 through the matching of the first sliding sleeve 12 and the first sliding rod 11, when the welding treatment is carried out on the heat exchanger, the positioning plate 20 can be pushed to move along the first sliding rod 11, so that the linear welding is carried out on the heat exchanger, and the welding trend is conveniently controlled; meanwhile, in the welding process, wind power is generated through the air blower, then the wind power generated by the air blower is transmitted to the hollow cavity 23 through the air guide pipe 30, when welding is carried out, the air blower externally connected with the air guide pipe 30 is opened, then the wind power generated by the air blower is transmitted into the hollow cavity 23 through the air guide pipe 30, then the wind power is blown out through the air exhaust hole 24, and the wind power is blown to the welding position, so that the welding bead after welding is cooled, the diffusion of heat generated in the welding process is reduced, the area where the heat is expanded is reduced, the surface precision of a welding part is improved, and the welding quality is improved.
It should be noted that although embodiments of the present invention have been shown and described, it will be appreciated by those skilled in the art that various changes, modifications, substitutions and alterations can be made in these embodiments without departing from the principles and spirit of the invention, the scope of which is defined in the appended claims and their equivalents.
Claims (10)
1. Heat exchanger welding bead rapid cooling device, including frame (10), locating plate (20) and air duct (30), its characterized in that: frame (10) inboard slidable mounting has locating plate (20), locating plate (20) surface center department runs through and has seted up constant head tank (21), well cavity (23) have all been seted up to the inside at locating plate (20) both ends, evenly seted up at the both ends of locating plate (20) lower surface runs through exhaust hole (24) of well cavity (23), locating plate (20) one side fixed mounting has runs through air duct (30) of well cavity (23), be close to on air duct (30) one side fixed mounting of locating plate (20) has control flap (31).
2. The quenching device for the bead of the heat exchanger as claimed in claim 1, wherein: frame (10) inboard symmetry fixed mounting has first slide bar (11), the equal fixed mounting in locating plate (20) both sides has the cooperation first sliding sleeve (12) of first slide bar (11), locating plate (20) pass through first sliding sleeve (12) and first slide bar (11) cooperation slidable mounting be in frame (10) are inboard.
3. The quenching device for the bead of the heat exchanger as claimed in claim 1, wherein: four corners of the lower surface of the frame (10) are all provided with a base (13) in a threaded manner.
4. The quenching device for the bead of the heat exchanger as claimed in claim 1, wherein: and clamping plates (40) are symmetrically and slidably mounted in the positioning grooves (21).
5. The quenching device for the bead of the heat exchanger as claimed in claim 4, wherein: the equal fixed mounting in both ends of constant head tank (21) inside has second slide bar (27), the equal fixed mounting in grip block (40) both ends has the cooperation second sliding sleeve (41) of second slide bar (27), grip block (40) pass through second sliding sleeve (41) and second slide bar (27) cooperation slidable mounting are in inside constant head tank (21).
6. The quenching device for the bead of the heat exchanger as claimed in claim 4, wherein: locating plate (20) surface is located the both sides of constant head tank (21) are all run through and have been seted up movable groove (22), movable groove (22) internal thread is installed and is run through screw lead screw (25) of constant head tank (21), screw lead screw (25) are located the inside one end of constant head tank (21) with grip block (40) rotate and are connected.
7. The quenching device for the bead of the heat exchanger as claimed in claim 6, wherein: and a turntable (26) is fixedly arranged at one end of the threaded screw rod (25) positioned in the movable groove (22).
8. The quenching device for the bead of the heat exchanger as claimed in claim 6, wherein: the thread screw rod (25) is located the inside one end of constant head tank (21) is provided with smooth end, the center department fixed mounting at the grip block (40) back has the cooperation the axle sleeve of smooth end, thread screw rod (25) pass through smooth end with the axle sleeve cooperation with grip block (40) rotate to be connected.
9. The quenching device for the bead of the heat exchanger as claimed in claim 2, wherein: the hollow cavity (23) is perpendicular to the first sliding rod (11).
10. The quenching device for the bead of the heat exchanger as claimed in claim 1, wherein: cavity (23) are provided with two, two cavity (23) parallel arrangement, one cavity (23) set up in the inside of locating plate (20) front end, another cavity (23) set up in the inside of locating plate (20) rear end.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210128859.5A CN114310065B (en) | 2022-02-11 | 2022-02-11 | Heat exchanger welding bead rapid cooling device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210128859.5A CN114310065B (en) | 2022-02-11 | 2022-02-11 | Heat exchanger welding bead rapid cooling device |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN114310065A true CN114310065A (en) | 2022-04-12 |
| CN114310065B CN114310065B (en) | 2022-12-06 |
Family
ID=81029806
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210128859.5A Active CN114310065B (en) | 2022-02-11 | 2022-02-11 | Heat exchanger welding bead rapid cooling device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114310065B (en) |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5902497A (en) * | 1994-10-18 | 1999-05-11 | Thyssen Industrie Ag | Process and device for cooling the area of a weld during laser welding |
| CN1739901A (en) * | 2005-09-28 | 2006-03-01 | 中国航空工业第一集团公司北京航空制造工程研究所 | Laser welding method and device with medium cooling |
| CN202199906U (en) * | 2011-05-11 | 2012-04-25 | 中国海洋大学 | Welding device for cold arc welding of thin plate gas shielded welding |
| CN110899921A (en) * | 2019-12-23 | 2020-03-24 | 兰州理工大学 | Welding-following chilling device for controlling welding deformation and welding method |
| CN210334879U (en) * | 2019-07-18 | 2020-04-17 | 上海纳特汽车零部件有限公司 | Manipulator for welding automobile parts |
| CN210848913U (en) * | 2019-11-18 | 2020-06-26 | 常州市鹏瑞自动化设备有限公司 | Welding robot with heat dissipation function |
| CN211162570U (en) * | 2019-11-08 | 2020-08-04 | 东莞市中亚电缆有限公司 | Copper pipe welding gun clamping and adjusting equipment |
| CN113369635A (en) * | 2021-06-30 | 2021-09-10 | 温州大学 | Multi-electric-arc coaxial heating efficient welding system |
-
2022
- 2022-02-11 CN CN202210128859.5A patent/CN114310065B/en active Active
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5902497A (en) * | 1994-10-18 | 1999-05-11 | Thyssen Industrie Ag | Process and device for cooling the area of a weld during laser welding |
| CN1739901A (en) * | 2005-09-28 | 2006-03-01 | 中国航空工业第一集团公司北京航空制造工程研究所 | Laser welding method and device with medium cooling |
| CN202199906U (en) * | 2011-05-11 | 2012-04-25 | 中国海洋大学 | Welding device for cold arc welding of thin plate gas shielded welding |
| CN210334879U (en) * | 2019-07-18 | 2020-04-17 | 上海纳特汽车零部件有限公司 | Manipulator for welding automobile parts |
| CN211162570U (en) * | 2019-11-08 | 2020-08-04 | 东莞市中亚电缆有限公司 | Copper pipe welding gun clamping and adjusting equipment |
| CN210848913U (en) * | 2019-11-18 | 2020-06-26 | 常州市鹏瑞自动化设备有限公司 | Welding robot with heat dissipation function |
| CN110899921A (en) * | 2019-12-23 | 2020-03-24 | 兰州理工大学 | Welding-following chilling device for controlling welding deformation and welding method |
| CN113369635A (en) * | 2021-06-30 | 2021-09-10 | 温州大学 | Multi-electric-arc coaxial heating efficient welding system |
Also Published As
| Publication number | Publication date |
|---|---|
| CN114310065B (en) | 2022-12-06 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO2021139029A1 (en) | Clamp for rotary shaft welding | |
| CN114310065B (en) | Heat exchanger welding bead rapid cooling device | |
| CN117697260B (en) | Block terminal box welding set that power supply was used | |
| CN221891517U (en) | Gear cutting machine convenient for uniform cooling | |
| CN218487631U (en) | Groove welding frock with angle adjustment structure | |
| CN207757094U (en) | A kind of laser soldering device with refrigerating function | |
| CN220943113U (en) | Cooling roller way of continuous casting machine | |
| CN221834012U (en) | A workpiece flushing and cooling device for the grinding area of a vertical grinder | |
| CN119457480A (en) | Laser cutting assembly and laser cutting device | |
| CN217193382U (en) | A Welding Water-cooled Laser Tailored Welding Device | |
| CN210703250U (en) | A welding automatic cooling line | |
| CN211219161U (en) | Multi-station laser welding equipment for automobile parts | |
| CN209681713U (en) | An intercooler air chamber fixture | |
| CN221848980U (en) | Laser welding machine with air cooling and wind power adjustment | |
| CN215747251U (en) | Aluminum radiator radiating tube welding device | |
| CN113001017A (en) | Cold air flow-channeling heat dissipation type laser welding equipment | |
| CN220579332U (en) | Double-layer efficient air-cooling quenching device | |
| CN222588388U (en) | Laser welding machine with easy adjustment of clamping angle | |
| CN217913359U (en) | High-frequency butt-joint welding machine is used in processing of new energy automobile battery package compact | |
| CN222344580U (en) | Steel band welding set is used in galvanized sheet processing | |
| CN218026299U (en) | Galvanized wire production cooling device | |
| CN222001944U (en) | A short slot shaft precision processing equipment | |
| CN221363298U (en) | Multidirectional welding head for laser welding machine | |
| CN224196180U (en) | Pulse servo hot riveting welding equipment | |
| CN222307788U (en) | Heat shield fixing device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |