CN113942136A - Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof - Google Patents
Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof Download PDFInfo
- Publication number
- CN113942136A CN113942136A CN202111003045.0A CN202111003045A CN113942136A CN 113942136 A CN113942136 A CN 113942136A CN 202111003045 A CN202111003045 A CN 202111003045A CN 113942136 A CN113942136 A CN 113942136A
- Authority
- CN
- China
- Prior art keywords
- fixed
- gear
- sliding
- motor
- parts
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 230000000844 anti-bacterial effect Effects 0.000 title claims abstract description 44
- 239000004033 plastic Substances 0.000 title claims abstract description 38
- 238000002360 preparation method Methods 0.000 title claims abstract description 25
- 238000002156 mixing Methods 0.000 claims abstract description 49
- 239000004743 Polypropylene Substances 0.000 claims abstract description 39
- 239000004793 Polystyrene Substances 0.000 claims abstract description 39
- 238000001125 extrusion Methods 0.000 claims abstract description 26
- 239000002994 raw material Substances 0.000 claims abstract description 25
- 239000004594 Masterbatch (MB) Substances 0.000 claims abstract description 16
- 239000004014 plasticizer Substances 0.000 claims abstract description 9
- 229920000168 Microcrystalline cellulose Polymers 0.000 claims abstract description 8
- 230000002745 absorbent Effects 0.000 claims abstract description 8
- 239000002250 absorbent Substances 0.000 claims abstract description 8
- 239000003963 antioxidant agent Substances 0.000 claims abstract description 8
- 230000003078 antioxidant effect Effects 0.000 claims abstract description 8
- 239000008108 microcrystalline cellulose Substances 0.000 claims abstract description 8
- 235000019813 microcrystalline cellulose Nutrition 0.000 claims abstract description 8
- 229940016286 microcrystalline cellulose Drugs 0.000 claims abstract description 8
- 230000003449 preventive effect Effects 0.000 claims abstract description 7
- 239000012745 toughening agent Substances 0.000 claims abstract description 5
- 238000005469 granulation Methods 0.000 claims abstract description 4
- 230000003179 granulation Effects 0.000 claims abstract description 4
- 239000000463 material Substances 0.000 claims abstract description 4
- -1 polypropylene Polymers 0.000 claims abstract description 4
- 229920001155 polypropylene Polymers 0.000 claims abstract description 4
- 229920002223 polystyrene Polymers 0.000 claims abstract description 4
- 230000007246 mechanism Effects 0.000 claims description 24
- 238000000034 method Methods 0.000 claims description 18
- 239000003638 chemical reducing agent Substances 0.000 claims description 16
- 238000007599 discharging Methods 0.000 claims description 16
- 238000011049 filling Methods 0.000 claims description 16
- 238000001514 detection method Methods 0.000 claims description 15
- 238000003756 stirring Methods 0.000 claims description 9
- 230000009467 reduction Effects 0.000 claims description 3
- 229910001220 stainless steel Inorganic materials 0.000 claims description 3
- 239000010935 stainless steel Substances 0.000 claims description 3
- 239000003795 chemical substances by application Substances 0.000 abstract description 3
- 230000008569 process Effects 0.000 description 14
- 239000003242 anti bacterial agent Substances 0.000 description 10
- 241000894006 Bacteria Species 0.000 description 4
- 239000000654 additive Substances 0.000 description 2
- 244000052616 bacterial pathogen Species 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 230000006872 improvement Effects 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000007480 spreading Effects 0.000 description 2
- 238000003892 spreading Methods 0.000 description 2
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 1
- 229910010413 TiO 2 Inorganic materials 0.000 description 1
- 238000012644 addition polymerization Methods 0.000 description 1
- 230000000996 additive effect Effects 0.000 description 1
- 238000009395 breeding Methods 0.000 description 1
- 230000001488 breeding effect Effects 0.000 description 1
- 150000001875 compounds Chemical class 0.000 description 1
- 238000003912 environmental pollution Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 229910021389 graphene Inorganic materials 0.000 description 1
- 230000036541 health Effects 0.000 description 1
- 230000005764 inhibitory process Effects 0.000 description 1
- 238000004898 kneading Methods 0.000 description 1
- 230000007774 longterm Effects 0.000 description 1
- 239000000314 lubricant Substances 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 239000000178 monomer Substances 0.000 description 1
- 239000002114 nanocomposite Substances 0.000 description 1
- NCXMLFZGDNKEPB-FFPOYIOWSA-N natamycin Chemical compound O[C@H]1[C@@H](N)[C@H](O)[C@@H](C)O[C@H]1O[C@H]1/C=C/C=C/C=C/C=C/C[C@@H](C)OC(=O)/C=C/[C@H]2O[C@@H]2C[C@H](O)C[C@](O)(C[C@H](O)[C@H]2C(O)=O)O[C@H]2C1 NCXMLFZGDNKEPB-FFPOYIOWSA-N 0.000 description 1
- 229960003255 natamycin Drugs 0.000 description 1
- 235000010298 natamycin Nutrition 0.000 description 1
- 239000004311 natamycin Substances 0.000 description 1
- 238000000053 physical method Methods 0.000 description 1
- 239000000049 pigment Substances 0.000 description 1
- 238000006068 polycondensation reaction Methods 0.000 description 1
- 239000003381 stabilizer Substances 0.000 description 1
- 230000001954 sterilising effect Effects 0.000 description 1
- 238000004659 sterilization and disinfection Methods 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 239000000057 synthetic resin Substances 0.000 description 1
- 229920003002 synthetic resin Polymers 0.000 description 1
- 230000007306 turnover Effects 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B9/00—Making granules
- B29B9/02—Making granules by dividing preformed material
- B29B9/06—Making granules by dividing preformed material in the form of filamentary material, e.g. combined with extrusion
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B7/00—Mixing; Kneading
- B29B7/02—Mixing; Kneading non-continuous, with mechanical mixing or kneading devices, i.e. batch type
- B29B7/06—Mixing; Kneading non-continuous, with mechanical mixing or kneading devices, i.e. batch type with movable mixing or kneading devices
- B29B7/10—Mixing; Kneading non-continuous, with mechanical mixing or kneading devices, i.e. batch type with movable mixing or kneading devices rotary
- B29B7/18—Mixing; Kneading non-continuous, with mechanical mixing or kneading devices, i.e. batch type with movable mixing or kneading devices rotary with more than one shaft
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B7/00—Mixing; Kneading
- B29B7/02—Mixing; Kneading non-continuous, with mechanical mixing or kneading devices, i.e. batch type
- B29B7/22—Component parts, details or accessories; Auxiliary operations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/265—Support structures or bases for apparatus, e.g. frames
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/285—Feeding the extrusion material to the extruder
- B29C48/288—Feeding the extrusion material to the extruder in solid form, e.g. powder or granules
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L25/00—Compositions of, homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by an aromatic carbocyclic ring; Compositions of derivatives of such polymers
- C08L25/02—Homopolymers or copolymers of hydrocarbons
- C08L25/04—Homopolymers or copolymers of styrene
- C08L25/06—Polystyrene
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
Abstract
The invention provides a long-acting antibacterial mildew-proof PP/PS plastic and a preparation method thereof, wherein the long-acting antibacterial mildew-proof PP/PS plastic is prepared from the following raw materials in parts by weight: 120-165 parts of PP (polypropylene) master batch, 240 parts of PS (polystyrene) master batch, 6-13 parts of antibacterial mildew preventive, 6-9 parts of microcrystalline cellulose, 2-4 parts of plasticizer, 1-5 parts of toughening agent, 1-5 parts of antioxidant and 1-3 parts of ultraviolet absorbent; the preparation method comprises the following steps: s1, adding the raw materials into a double-screw extruder according to the proportion for mixing and extruding; s2, conveying the material extruded in the step S1 to a single-screw extruder for granulation to obtain a finished product. The long-acting antibacterial mildew-proof PP/PS plastic is prepared from the PP master batch, the PS master batch, the antibacterial mildew-proof agent, microcrystalline cellulose, the plasticizer, the toughening agent, the antioxidant and the ultraviolet absorbent, and the raw materials are premixed before entering the shell of the extruder to improve the mixing uniformity and reduce the mixing time in the extrusion screw.
Description
Technical Field
The invention relates to the technical field of plastic preparation, in particular to a long-acting antibacterial mildew-proof PP/PS plastic and a preparation method thereof.
Background
The plastic is a high molecular compound which is polymerized by addition polymerization or polycondensation reaction by taking a monomer as a raw material, has moderate deformation resistance and is between fibers and rubber, and consists of synthetic resin, fillers, plasticizers, stabilizers, lubricants, pigments and other additives; along with the progress of human society, plastic products occupy more and more important positions in daily life, meanwhile, various environmental pollutions are increasingly serious, the plastic products are easily polluted by bacteria in the long-term use process, the spreading and spreading of harmful bacteria are directly caused, and the health of people is harmed, the antibacterial plastic is that antibacterial agents are added into the plastic, so that the plastic has antibacterial property, the bacteria stained on the plastic can be killed or inhibited within a certain time, and compared with the conventional chemical and physical methods, the antibacterial plastic has long sterilization time, and is economical and convenient; the antibacterial agent is used as an additive and can effectively inhibit the breeding of bacteria. Plastic antibacterial agents are generally classified into inorganic antibacterial agents, organic antibacterial agents, natural antibacterial agents and complex antibacterial agents. Because different antibacterial agents have different antibacterial action mechanisms and effectiveness on the same pathogenic bacteria and different antibacterial action mechanisms and inhibition ranges of the same antibacterial agent on different pathogenic bacteria, the antibacterial agent which is long-acting, broad-spectrum, high-efficiency and safe is researched, and the research on the antibacterial mechanism is very important;
in the existing preparation process of the long-acting antibacterial mildew-proof PP/PS plastic, a double-screw extruder is needed to mix the raw materials, the mixing efficiency of the raw materials is improved, however, when the existing double-screw extruder is used, the mixing efficiency between the raw materials is low, so that the raw materials are uniformly mixed when a long extruding screw is required to be arranged, the manufacturing cost is high, in addition, when the existing double-screw extruder is maintained, the shell of the extruder and the extruding screw rod need to be disassembled, and because the matching degree between the shell and the extruding screw rod is higher, therefore, when in disassembly, the moving stability is required to be kept all the time, if the field is uneven, the equipment is easy to damage, therefore, the requirement on the flatness of the ground is higher, the arrangement of the equipment is not facilitated, in the case of a preparation method which is relatively more complete, it is necessary to combine the method from the whole process of the process flow such as the improvement of the equipment to be more beneficial to the improvement of the whole process flow.
Therefore, it is necessary to provide a long-acting antibacterial and mildewproof PP/PS plastic and a preparation method thereof to solve the technical problems.
Disclosure of Invention
In order to solve the technical problems, the invention provides a long-acting antibacterial mildew-proof PP/PS plastic and a preparation method thereof.
The invention provides a preparation method of long-acting antibacterial and mildewproof PP/PS plastic, which comprises the following steps:
s1, adding the PP master batch, the PS master batch, the antibacterial mildew preventive, the microcrystalline cellulose, the plasticizer, the flexibilizer, the antioxidant and the ultraviolet absorbent into a double-screw extruder according to the proportion, and mixing and extruding;
s2, conveying the material extruded in the step S1 to a single-screw extruder for extrusion granulation, so as to obtain the long-acting antibacterial mildew-proof PP/PS plastic;
wherein, in the step S1, the twin-screw extruder comprises a support table, fixing feet, a translation mechanism, a quantitative blanking channel, a mixing blanking hopper, a flatness detection device, an adjusting and supporting device, an equipment box, a speed reducer, a driving motor, a translation groove, a sliding groove, a support seat, an extruder shell, an extrusion screw, a first gear and a blanking nozzle, wherein the fixing feet are symmetrically fixed at the bottom of the support table, the equipment box is fixed at one end of the upper surface of the support table, the speed reducer is fixed at one end of the upper surface of the support table, the driving motor is fixed at the top of the speed reducer, the output end of the driving motor is clamped with the input end of the speed reducer, the translation groove is arranged in the middle of the support table, the sliding grooves are symmetrically arranged at two sides of the translation groove, the translation mechanism is arranged on the inner wall of the translation groove, the support seat is fixed at the top of the translation mechanism, the extruder shells are fixed at the tops of the two support seats, the inner wall of the extruder shell is symmetrically and rotatably connected with two extrusion screws which are matched with each other through a bearing, one end of each extrusion screw penetrates through the extruder shell and is fixed with a first gear, the two first gears are meshed and connected, the output end of the speed reducer is fixedly connected with one extrusion screw through a coupler, one end of the extruder shell is hinged with a blanking nozzle, a quantitative blanking channel is fixed at a feeding hole of the extruder shell, a mixed blanking hopper is fixed at the top of the quantitative blanking channel, a flatness detection device is symmetrically fixed at one end of the translation mechanism, and an adjusting and supporting device is fixed at one end of the translation mechanism, which is close to the flatness detection device;
translation mechanism includes sliding block, first crossbeam, second crossbeam, fixed plate, first threaded rod, first motor and bracing piece, sliding tray inner wall sliding connection has the sliding block, two sliding block both ends symmetry is fixed with first crossbeam and second crossbeam, first crossbeam middle part set up threaded hole, translation inslot wall symmetry is fixed with the fixed plate, two the fixed plate middle part is rotated through the bearing and is connected with first threaded rod, and first threaded rod and first crossbeam middle part threaded connection, one fixed plate one side is fixed with first motor, the output and the first threaded rod fixed connection of first motor, first crossbeam and second crossbeam top symmetry are fixed with the bracing piece, and bracing piece and supporting seat fixed connection.
Preferably, ration unloading passageway includes unloading pipe, filling block, first pivot, flitch and second motor down, the feed inlet of extruder shell is fixed with the unloading pipe, unloading inside pipe wall symmetry is fixed with the filling block, and the filling block middle part is the arc setting, the unloading inside pipe wall rotates through the bearing and is connected with first pivot, first pivot outside equidistance is fixed with the unloading board, and the unloading board is located two the filling block middle part, and the arcwall sliding contact in unloading board tip and the filling block, unloading pipe one side is fixed with the second motor, and the output and the first pivot fixed connection of second motor.
Preferably, the mixing blanking hopper comprises a mixing bin, a second rotating shaft, a third rotating shaft, a second gear, a third gear, a fourth gear, a fifth gear, a first mounting plate, a third motor and a stirring rod, the top of the blanking pipe is fixedly provided with the mixing bin, the mixing bin is communicated with the blanking pipe, the upper end of the inner wall of the mixing bin is symmetrically and rotatably connected with the second rotating shaft through a bearing, the lower end of the inner wall of the mixing bin is rotatably connected with the third rotating shaft through the bearing, one end of the second rotating shaft penetrates through the mixing bin and is fixedly provided with the second gear, one side of the mixing bin, which is close to the second gear, is rotatably connected with the third gear through an axial symmetry shaft, the two third gears are respectively meshed with the two second gears and are mutually meshed and connected, one end of the third rotating shaft is fixedly provided with the fourth gear, one side of the mixing bin is rotatably connected with the fifth gear through a shaft, and the fifth gear is connected with the fourth gear engagement, the fifth gear is with one the third gear engagement is connected, it is fixed with first mounting panel to mix storehouse one side, first mounting panel top is fixed with the third motor, and the output and the third pivot fixed connection of third motor, the equal equidistance in second pivot and the third pivot outside is fixed with the puddler.
Preferably, the flatness detection device comprises an L-shaped rod, a first chute, a first slider, a first slide bar, a first U-shaped plate, a first roller, a spring, a groove, a rack, a sixth gear and a coder, wherein the L-shaped rod is symmetrically fixed on one side of the second beam, the first chute is formed at one end of the L-shaped rod, a first through hole is formed at the bottom of the inner wall of the first chute, the first slider is slidably connected to the inner wall of the first chute, the first slide bar is fixed at the bottom of the first slider, the first U-shaped plate is fixed at the bottom of the first slide bar through the first through hole, the first roller is rotatably connected to the inner wall of the first U-shaped plate through a shaft, the spring is fixed at the inner wall of the first chute, the bottom of the spring is fixedly connected to the first slider, the groove is formed at the upper end of the L-shaped plate, a second through hole is formed at one end of the groove, and the second through hole is respectively communicated with the first chute and the outside, the utility model discloses a recess, including first slider, second through-hole inner wall sliding connection has the rack, and rack and first slider fixed connection, the recess inner wall rotates through the bearing and is connected with the sixth gear, and the meshing of sixth gear and rack is connected, L shape pole one end is fixed with the encoder, and the input and the sixth gear middle part fixed connection of encoder.
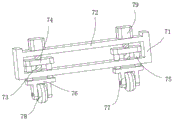
Preferably, the adjusting and supporting device comprises a U-shaped frame, a connecting plate, a second threaded rod, a sliding plate, a second sliding rod, a second mounting plate, a third mounting plate, a second idler wheel and a fourth motor, the bottom of the second cross beam is fixed with the U-shaped frame, the upper end of the inner wall of the U-shaped frame is fixed with the connecting plate, the inner wall of the connecting plate and the inner wall of the U-shaped frame are connected with the second threaded rod through symmetrical rotation of bearings, the inner wall of the U-shaped frame is symmetrically and slidably connected with the sliding plate, the middle part of the sliding plate is provided with threads, the sliding plate is in threaded connection with the second threaded rod, the two ends of the sliding plate are symmetrically fixed with the second sliding rod, the second sliding rod is in sliding connection with the U-shaped frame through a sliding hole, the bottoms of the second sliding rods penetrate through the U-shaped frame and are fixed with the second mounting plate, the lower surface of the second mounting plate is symmetrically fixed with the third mounting plate, and the middle parts of the two third mounting plates are connected with the second idler wheel through rotation of shafts, and the top of the connecting plate is symmetrically fixed with a fourth motor, and the output end of the fourth motor is fixedly connected with the second threaded rod.
Preferably, the first roller and the second roller are made of stainless steel, the first roller and the second roller are provided with rubber layers, and the thickness of each rubber layer is 2 mm.
Preferably, one end of the extruder shell, which is close to the feeding nozzle, is hinged with a hydraulic cylinder through a shaft pin, the output end of the hydraulic cylinder is hinged with one end of the feeding nozzle through the shaft pin, and the extruder shell and the feeding nozzle are fixedly connected through a flange.
Preferably, the fixed foot is L-shaped and is fixedly connected with the ground through a bolt.
Preferably, the first motor, the second motor, the third motor and the fourth motor are all speed reduction motors.
According to the method, the invention also comprises a long-acting antibacterial mildew-proof PP/PS plastic which is prepared from the following raw materials in parts by weight: 120-165 parts of PP (polypropylene) master batch, 240 parts of PS (polystyrene) master batch, 6-13 parts of antibacterial mildew preventive, 6-9 parts of microcrystalline cellulose, 2-4 parts of plasticizer, 1-5 parts of toughening agent, 1-5 parts of antioxidant and 1-3 parts of ultraviolet absorbent.
The long-acting antibacterial mildew-proof PP/PS plastic and the preparation method thereof provided by the invention have the following beneficial effects:
the invention provides a long-acting antibacterial mildew-proof PP/PS plastic and a preparation method thereof, wherein the preparation method comprises the following steps:
1. when in use, the raw materials are added into the mixing bin, the third rotating shaft is driven to rotate by the rotation of the third motor, and then the fourth gear can be driven to rotate, so that the fourth gear drives the third gear to rotate by the fifth gear, the two third gears are meshed with each other, so that the two third gears rotate in opposite directions, and then the two second gears rotate in opposite directions, so that the two second rotating shafts rotate in opposite directions, so that the third motor simultaneously drives the stirring rods on the second rotating shaft and the third rotating shaft to rotate simultaneously, the raw materials are stirred, the stirred raw materials fall between the two blanking plates, then the first rotating shaft is driven to rotate by the rotation of the second motor, the raw materials between the blanking plates are driven to rotate, so that the raw materials are conveyed downwards to the interior of the extruder shell to be mixed, and the device is premixed before the raw materials enter the extruder shell, and the mixing uniformity is greatly improved, therefore, the mixing time in the extrusion screw can be reduced, and the working efficiency is improved;
2. when the extruder shell and the extrusion screw rod need to be disassembled and maintained, the first motor rotates to drive the first threaded rod to rotate, and further the first cross beam can be driven to move, so that the first cross beam drives the sliding block and the second cross beam to move, and further the extruder shell can be driven to move towards one end, when the extruder shell moves, the first roller on the flatness detection device on the second cross beam and the second roller on the adjusting and supporting device contact with the ground to roll, and the second cross beam is supported by the second roller, if the ground is uneven, the first roller firstly contacts with the ground, the first roller is always applied with downward force by the spring, so that the first roller can move up and down along with the ground height, and further the first slider drives the rack to lift, so that the rack drives the sixth gear to rotate, the rotation angle of the sixth gear is recorded by the encoder, and the rotation angle of the sixth gear is in direct proportion to the lifting distance of the rack, therefore, the lifting height of the first roller can be calculated, the height of the ground fluctuation can be calculated and recorded, in the process that the second beam continuously moves forwards, the second roller moves along the path of the first roller, and when the second roller moves to the position of the first roller, the fourth motor rotates to drive the second threaded rod to rotate, so that the sliding plate can be driven to lift, the second sliding rod drives the second roller on the second mounting plate to lift, the height of the second roller is adjusted to compensate the height of the road surface, so that the second beam can be always kept at the same horizontal height in the moving process, the sliding stability of the sliding block is improved, the stability of the extruder shell in moving is improved, the extruder shell is prevented from generating larger fluctuation and shaking during moving, the extrusion damage between the extruder shell and the extruder screw is avoided, the stability is improved, and the device is convenient for moving and dismounting the extruder shell, and the movement is stable, the extruder shell and the extrusion screw are prevented from being damaged, the requirement on the field flatness is reduced, and the equipment is convenient to arrange.
Drawings
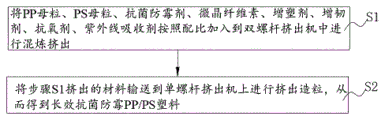
FIG. 1 is a schematic flow chart of a preparation method provided by the present invention;
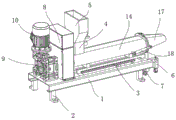
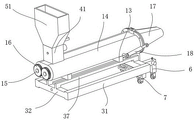
FIG. 2 is a schematic view of the overall structure provided by the present invention;
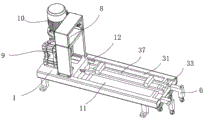
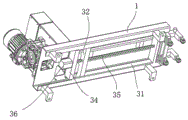
FIG. 3 is a schematic view of a sliding slot structure provided in the present invention;
FIG. 4 is a schematic structural view of a translation mechanism provided in the present invention;
FIG. 5 is a schematic structural diagram of an extruder housing provided by the present invention;
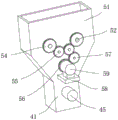
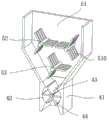
FIG. 6 is a schematic structural view of a mixing and feeding mechanism according to the present invention;
FIG. 7 is a schematic view of a quantitative blanking channel structure provided by the present invention;
FIG. 8 is a schematic view of a slider structure according to the present invention;
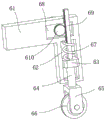
FIG. 9 is a schematic structural diagram of a flatness detecting apparatus according to the present invention;
FIG. 10 is a schematic view of the internal structure of an L-shaped pole provided by the present invention;
fig. 11 is a schematic structural view of an adjusting and supporting device provided by the present invention.
Reference numbers in the figures: 1. a support table; 2. a fixing leg; 3. a translation mechanism; 31. a slider; 32. a first cross member; 33. a second cross member; 34. a fixing plate; 35. a first threaded rod; 36. a first motor; 37. a support bar; 4. a quantitative blanking channel; 41. a discharging pipe; 42. filling blocks; 43. a first rotating shaft; 44. a blanking plate; 45. a second motor; 5. a mixing discharge hopper; 51. a mixing bin; 52. a second rotating shaft; 53. a third rotating shaft; 54. a second gear; 55. a third gear; 56. a fourth gear; 57. a fifth gear; 58. a first mounting plate; 59. a third motor; 510. a stirring rod; 6. a flatness detection device; 61. an L-shaped rod; 62. a first chute; 63. a first slider; 64. a first slide bar; 65. a first U-shaped plate; 66. a first roller; 67. a spring; 68. a groove; 69. a rack; 610. a sixth gear; 611. an encoder; 7. adjusting the support device; 71. a U-shaped frame; 72. a connecting plate; 73. a second threaded rod; 74. a slide plate; 75. a second slide bar; 76. a second mounting plate; 77. a third mounting plate; 78. a second roller; 79. a fourth motor; 8. an equipment box; 9. a speed reducer; 10. a drive motor; 11. a translation slot; 12. a sliding groove; 13. a supporting seat; 14. an extruder housing; 15. extruding a screw; 16. a first gear; 17. a discharging nozzle; 18. and a hydraulic cylinder.
Detailed Description
The invention is further described with reference to the following figures and embodiments.
In the specific implementation process, as shown in fig. 1-5, a preparation method of the long-acting antibacterial mildew-proof PP/PS plastic is completed by matching a double-screw extruder, and the preparation method comprises the following steps:
s1, adding the PP master batch, the PS master batch, the antibacterial mildew preventive, the microcrystalline cellulose, the plasticizer, the flexibilizer, the antioxidant and the ultraviolet absorbent into a double-screw extruder according to the proportion, and mixing and extruding;
s2, conveying the material extruded in the step S1 to a single-screw extruder for extrusion granulation, so as to obtain the long-acting antibacterial mildew-proof PP/PS plastic; the "S1" and "S2" marks specifically indicate "step one" and "step two";
the four temperature sections in the mixing and extruding process are as follows: the feeding section 110-120 ℃, the conveying section 125-135 ℃, the melting section 135-145 ℃ and the extrusion section 140-150 ℃;
wherein the twin-screw extruder used in the step S1 comprises a supporting table 1, fixing legs 2, a translation mechanism 3, a quantitative blanking channel 4, a mixed blanking hopper 5, a flatness detection device 6, an adjusting and supporting device 7, an equipment box 8, a speed reducer 9, a driving motor 10, a translation groove 11, a sliding groove 12, a supporting seat 13, an extruder shell 14, an extrusion screw 15, a first gear 16 and a blanking nozzle 17, wherein the fixing legs 2 are symmetrically fixed at the bottom of the supporting table 1, the fixing legs 2 are arranged in an L shape, the fixing legs 2 are fixedly connected with the ground through bolts, the equipment box 8 is fixed at one end of the upper surface of the supporting table 1, the speed reducer 9 is fixed at one end of the upper surface of the supporting table 1, the driving motor 10 is fixed at the top of the speed reducer 9, the output end of the driving motor 10 is clamped with the input end of the speed reducer 9, the translation groove 11 is arranged in the middle of the supporting table 1, the two sides of the translation groove 11 are symmetrically provided with sliding grooves 12, the inner wall of the translation groove 11 is provided with a translation mechanism 3, the top of the translation mechanism 3 is fixed with a support base 13, the tops of the two support bases 13 are fixed with an extruder shell 14, the inner wall of the extruder shell 14 is symmetrically and rotatably connected with two extrusion screws 15 which are matched with each other through bearings, one end of each extrusion screw 15 penetrates through the extruder shell 14 and is fixed with a first gear 16, the two first gears 16 are meshed and connected, the output end of the speed reducer 9 is fixedly connected with one extrusion screw 15 through a coupler, one end of the extruder shell 14 is hinged with a blanking nozzle 17, a feed inlet of the extruder shell 14 is fixed with a quantitative blanking channel 4, the top of the quantitative blanking channel 4 is fixed with a mixed blanking hopper 5, and one end of the translation mechanism 3 is symmetrically fixed with a flatness detection device 6, an adjusting and supporting device 7 is fixed at one end of the translation mechanism 3 close to the flatness detection device 6;
referring to fig. 2-4, the translation mechanism 3 includes a sliding block 31, a first beam 32, a second beam 33, a fixed plate 34, a first threaded rod 35, a first motor 36 and a support rod 37, the inner wall of the sliding groove 12 is connected with sliding blocks 31 in a sliding way, two ends of each sliding block 31 are symmetrically fixed with a first beam 32 and a second beam 33, threaded holes are formed in the middle of the first cross beam 32, fixing plates 34 are symmetrically fixed on the inner wall of the translation groove 11, first threaded rods 35 are rotatably connected to the middle of the two fixing plates 34 through bearings, and the first threaded rod 35 is in threaded connection with the middle of the first beam 32, one side of one of the fixing plates 34 is fixed with a first motor 36, the output end of the first motor 36 is fixedly connected with a first threaded rod 35, support rods 37 are symmetrically fixed at the tops of the first beam 32 and the second beam 33, and the support rods 37 are fixedly connected with the support base 13;
referring to fig. 8-10, the flatness detecting apparatus 6 includes an L-shaped bar 61, a first sliding groove 62, a first sliding block 63, a first sliding rod 64, a first U-shaped plate 65, a first roller 66, a spring 67, a groove 68, a rack 69, a sixth gear 610 and an encoder 611, the L-shaped bar 61 is symmetrically fixed on one side of the second beam 33, the first sliding groove 62 is formed at one end of the L-shaped bar 61, a first through hole is formed at the bottom of the inner wall of the first sliding groove 62, the first sliding block 63 is slidably connected to the inner wall of the first sliding groove 62, the first sliding bar 64 is fixed at the bottom of the first sliding block 63, the first U-shaped plate 65 is fixed at the bottom of the first sliding bar 64 through the first through hole, the first roller 66 is rotatably connected to the inner wall of the first U-shaped plate 65 through a shaft, the spring 67 is fixed at the inner wall of the first sliding groove 62, and the bottom of the spring 67 is fixedly connected to the first sliding block 63, a groove 68 is formed in the upper end of the L-shaped plate, a second through hole is formed in one end of the groove 68, the second through hole is respectively communicated with the first sliding groove 62 and the outside, a rack 69 is connected to the inner wall of the second through hole in a sliding manner, the rack 69 is fixedly connected with the first sliding block 63, a sixth gear 610 is rotatably connected to the inner wall of the groove 68 through a bearing, the sixth gear 610 is meshed with the rack 69, an encoder 611 is fixed to one end of the L-shaped rod 61, and the input end of the encoder 611 is fixedly connected with the middle of the sixth gear 610;
referring to fig. 11, the adjusting and supporting device 7 includes a U-shaped frame 71, a connecting plate 72, a second threaded rod 73, a sliding plate 74, a second sliding rod 75, a second mounting plate 76, a third mounting plate 77, a second roller 78 and a fourth motor 79, the bottom of the second beam 33 is fixed with the U-shaped frame 71, the upper end of the inner wall of the U-shaped frame 71 is fixed with the connecting plate 72, the inner walls of the connecting plate 72 and the U-shaped frame 71 are symmetrically and rotatably connected with the second threaded rod 73 through bearings, the inner walls of the U-shaped frame 71 are symmetrically and slidably connected with the sliding plate 74, the middle of the sliding plate 74 is provided with threads, the sliding plate 74 is in threaded connection with the second threaded rod 73, the two ends of the sliding plate 74 are symmetrically fixed with the second sliding rod 75, the second sliding rod 75 is slidably connected with the U-shaped frame 71 through sliding holes, the bottoms of the two second sliding rods 75 pass through the U-shaped frame 71 and are fixed with the second mounting plate 76, the lower surface of the second mounting plate 76 is symmetrically fixed with the third mounting plate 77, the middle parts of the two third mounting plates 77 are rotatably connected with second rollers 78 through shafts, fourth motors 79 are symmetrically fixed at the tops of the connecting plates 72, and the output ends of the fourth motors 79 are fixedly connected with second threaded rods 73;
it should be noted that when the extruder housing 14 and the extrusion screw 15 need to be disassembled and maintained, the first motor 36 rotates to drive the first threaded rod 35 to rotate, and further drive the first beam 32 to move, so that the first beam 32 drives the sliding block 31 and the second beam 33 to move, and further drive the extruder housing 14 to move towards one end, when moving, the first roller 66 on the flatness detection device 6 on the second beam 33 and the second roller 78 on the adjustment support device 7 contact with the ground to roll, and the second beam 33 is supported by the second roller 78, if the ground is uneven, the first roller 66 first contacts with the ground, the spring 67 always applies downward force to the first roller 66, so that the first roller 66 can move up and down along with the height of the ground, and further the first slider 63 drives the rack 69 to lift, so that the rack 69 drives the sixth gear 610 to rotate, the rotation angle of the sixth gear 610 is recorded by the encoder 611, and the rotation angle of the sixth gear 610 is in direct proportion to the lifting distance of the rack 69, so that the lifting height of the first roller 66 can be calculated, and the height of the ground surface is calculated and recorded, when the second beam 33 moves forward, the second roller 78 moves along the path of the first roller 66, and when the second roller 78 moves to the position of the first roller 66, the fourth motor 79 rotates to drive the second threaded rod 73 to rotate, and further the sliding plate 74 can be driven to lift, the second sliding rod 75 drives the second roller 78 on the second mounting plate 76 to lift, the height of the second roller 78 is adjusted, the height of the road surface is compensated, so that the second beam 33 can be kept at the same horizontal height all the time in the moving process, the sliding stability of the sliding block 31 is improved, and the stability of the extruder housing 14 during moving is improved, the extrusion damage between the extrusion screw 15 and the extruder shell 14 with large fluctuation and shaking during movement is avoided, and the stability is improved.
Referring to fig. 6 to 7, the quantitative discharging channel 4 includes a discharging pipe 41, a filling block 42, a first rotating shaft 43, a discharging plate 44 and a second motor 45, the discharging pipe 41 is fixed at a feeding port of the extruder housing 14, the filling blocks 42 are symmetrically fixed on an inner wall of the discharging pipe 41, the middle of each filling block 42 is arranged in an arc shape, the inner wall of the discharging pipe 41 is rotatably connected with the first rotating shaft 43 through a bearing, the discharging plates 44 are fixed on outer sides of the first rotating shaft 43 at equal intervals, the discharging plate 44 is located in the middle of the two filling blocks 42, an end of the discharging plate 44 is in sliding contact with an arc surface in the filling block 42, the second motor 45 is fixed on one side of the discharging pipe 41, and an output end of the second motor 45 is fixedly connected with the first rotating shaft 43;
referring to fig. 6-7, the mixing hopper 5 includes a mixing bin 51, a second rotating shaft 52, a third rotating shaft 53, a second gear 54, a third gear 55, a fourth gear 56, a fifth gear 57, a first mounting plate 58, a third motor 59 and a stirring rod 510, the mixing bin 51 is fixed on the top of the discharging pipe 41, the mixing bin 51 is communicated with the discharging pipe 41, the second rotating shaft 52 is symmetrically and rotatably connected to the upper end of the inner wall of the mixing bin 51 through a bearing, the third rotating shaft 53 is rotatably connected to the lower end of the inner wall of the mixing bin 51 through a bearing, the second gear 54 is fixed on one end of the second rotating shaft 52 passing through the mixing bin 51, the third gear 55 is rotatably connected to one side of the mixing bin 51 close to the second gear 54 through an axial symmetry, the two third gears 55 are respectively engaged with the two second gears 54, and the two third gears 55 are engaged with each other, a fourth gear 56 is fixed at one end of the third rotating shaft 53, a fifth gear 57 is rotatably connected to one side of the mixing bin 51 through a shaft, the fifth gear 57 is meshed with the fourth gear 56, the fifth gear 57 is meshed with one third gear 55, a first mounting plate 58 is fixed to one side of the mixing bin 51, a third motor 59 is fixed to the top of the first mounting plate 58, the output end of the third motor 59 is fixedly connected with the third rotating shaft 53, and stirring rods 510 are fixed to the outer sides of the second rotating shaft 52 and the third rotating shaft 53 at equal intervals;
it should be noted that, when in use, the raw materials are added into the mixing bin 51, the third motor 59 rotates to drive the third rotating shaft 53 to rotate, and further drives the fourth gear 56 to rotate, so that the fourth gear 56 drives the third gear 55 to rotate through the fifth gear 57, since the two third gears 55 are meshed with each other, the two third gears 55 rotate in opposite directions, and thus the two second gears 54 can be driven to rotate in opposite directions, so that the two second rotating shafts 52 rotate in opposite directions, the third motor 59 simultaneously drives the second rotating shafts 52 and the stirring rods 510 on the third rotating shafts 53 to rotate simultaneously, the raw materials are stirred, the stirred raw materials fall between the two blanking plates 44, then the first rotating shaft 43 is driven to rotate by the rotation of the second motor 45, the blanking plates 44 are driven to rotate, so that the raw material between the blanking plates 44 is conveyed downward to the inside of the extruder housing 14 for kneading.
The first roller 66 and the second roller 78 are made of stainless steel, the first roller 66 and the second roller 78 are provided with rubber layers, the thickness of each rubber layer is 2mm, deformation of the first roller 66 and the second roller 78 in force bearing is reduced, and precision is improved.
Referring to fig. 2, one end of the extruder housing 14 close to the blanking nozzle 17 is hinged to a hydraulic cylinder 18 through a shaft pin, an output end of the hydraulic cylinder 18 is hinged to one end of the blanking nozzle 17 through the shaft pin, the extruder housing 14 and the blanking nozzle 17 are fixedly connected through a flange, and when the blanking nozzle 17 is detached, after a bolt of the fixed flange is detached, the blanking nozzle 17 can be pushed to turn over through the hydraulic cylinder 18, so that the use is convenient.
The first motor 36, the second motor 45, the third motor 59 and the fourth motor 79 are all speed reduction motors.
The invention also comprises a long-acting antibacterial mildew-proof PP/PS plastic which is prepared from the following raw materials in parts by weight: 120-165 parts of PP (polypropylene) master batch, 240 parts of PS (polystyrene) master batch, 6-13 parts of antibacterial mildew preventive, 6-9 parts of microcrystalline cellulose, 2-4 parts of plasticizer, 1-5 parts of toughening agent, 1-5 parts of antioxidant and 1-3 parts of ultraviolet absorbent;
the antibacterial and mildewproof agent contains 2-5 wt% of graphene oxide/TiO 2 nano-composite and 3-7 wt% of natamycin, and the specific weight parts and the technical instructions of the antibacterial and mildewproof agent can be applied to the invention by the technical staff in the field according to the invention and the technical instructions of the prior art to realize the technical scheme of the invention, and are not described herein again.
In connection with the process of the present invention, the working principle of the twin-screw extruder in the process modification of the present invention is mainly provided to help those skilled in the art to understand the present invention more fully:
when in use, the raw materials are added into the mixing bin 51, the third rotating shaft 53 is driven to rotate by the rotation of the third motor 59, and then the fourth gear 56 can be driven to rotate, so that the fourth gear 56 drives the third gear 55 to rotate through the fifth gear 57, the two third gears 55 are driven to rotate in opposite directions due to the mutual engagement of the two third gears 55, and then the two second gears 54 are driven to rotate in opposite directions, so that the third motor 59 drives the second rotating shaft 52 and the stirring rod 510 on the third rotating shaft 53 to rotate simultaneously, the raw materials are stirred, the stirred raw materials fall between the two blanking plates 44, then the first rotating shaft 43 is driven to rotate by the rotation of the second motor 45, so that the raw materials between the blanking plates 44 are conveyed downwards to the interior of the extruder housing 14 for mixing, when the extruder housing 14 and the extrusion screw 15 need to be disassembled and maintained, the first motor 36 rotates to drive the first threaded rod 35 to rotate, and further drives the first beam 32 to move, so that the first beam 32 drives the sliding block 31 and the second beam 33 to move, and further drives the extruder housing 14 to move towards one end, when moving, the first roller 66 on the flatness detection device 6 on the second beam 33 and the second roller 78 on the adjusting and supporting device 7 on the second beam 33 contact and roll with the ground, and the second beam 33 is supported by the second roller 78, if the ground is uneven, the first roller 66 first contacts with the ground, the first roller 66 is always applied with downward force by the spring 67, so that the first roller 66 can move up and down along with the height of the ground, and further the first slider 63 drives the rack 69 to lift up and down, so that the rack 69 drives the sixth gear 610 to rotate, the rotation angle of the sixth gear 610 is recorded by the encoder 611, the rotation angle of the sixth gear 610 is in direct proportion to the lifting distance of the rack 69, therefore, the lifting height of the first roller 66 can be calculated, the height of the ground surface fluctuation can be calculated and recorded, in the process that the second beam 33 continues to move forwards, the second roller 78 moves along the path of the first roller 66, and when the second roller 78 moves to the position of the first roller 66, the fourth motor 79 rotates to drive the second threaded rod 73 to rotate, so that the sliding plate 74 can be driven to lift, the second sliding rod 75 drives the second roller 78 on the second mounting plate 76 to lift, the height of the second roller 78 is adjusted to compensate the height of the road surface, so that the second beam 33 can be always kept at the same horizontal height in the moving process, the sliding stability of the sliding block 31 is improved, the stability of the extruder housing 14 in moving is improved, and the extruder housing 14 is prevented from generating large fluctuation and shaking during moving and being damaged by extrusion between the extruder screw 15, the stability is improved.
The circuits and controls involved in the present invention are prior art and will not be described in detail herein.
The above description is only an embodiment of the present invention, and not intended to limit the scope of the present invention, and all modifications of equivalent structures and equivalent processes, which are made by using the contents of the present specification and the accompanying drawings, or directly or indirectly applied to other related technical fields, are included in the scope of the present invention.
Claims (10)
1. A preparation method of long-acting antibacterial mildew-proof PP/PS plastic is characterized by comprising the following steps:
s1, adding the PP master batch, the PS master batch, the antibacterial mildew preventive, the microcrystalline cellulose, the plasticizer, the flexibilizer, the antioxidant and the ultraviolet absorbent into a double-screw extruder according to the proportion, and mixing and extruding;
s2, conveying the material extruded in the step S1 to a single-screw extruder for extrusion granulation, so as to obtain the long-acting antibacterial mildew-proof PP/PS plastic;
wherein, in the step S1, the double-screw extruder comprises a supporting table (1), fixing feet (2), a translation mechanism (3), a quantitative blanking channel (4), a mixed blanking hopper (5), a flatness detection device (6), an adjusting and supporting device (7), an equipment box (8), a speed reducer (9), a driving motor (10), a translation groove (11), a sliding groove (12), a supporting seat (13), an extruder shell (14), an extrusion screw (15), a first gear (16) and a blanking nozzle (17), the bottom of the supporting table (1) is symmetrically fixed with the fixing feet (2), one end of the upper surface of the supporting table (1) is fixed with the equipment box (8), one end of the upper surface of the supporting table (1) is fixed with the speed reducer (9), the top of the speed reducer (9) is fixed with the driving motor (10), and the output end of the driving motor (10) is clamped with the input end of the speed reducer (9), the automatic feeding device is characterized in that a translation groove (11) is formed in the middle of the supporting table (1), sliding grooves (12) are symmetrically formed in two sides of the translation groove (11), a translation mechanism (3) is installed on the inner wall of the translation groove (11), a supporting seat (13) is fixed at the top of the translation mechanism (3), an extruder shell (14) is fixed at the top of the supporting seat (13), two extrusion screws (15) which are matched with each other are rotatably connected to the inner wall of the extruder shell (14) through bearings in a symmetrical mode, one end of each extrusion screw (15) penetrates through the extruder shell (14) and is fixed with a first gear (16), the two first gears (16) are connected in a meshed mode, the output end of the speed reducer (9) is fixedly connected with one extrusion screw (15) through a coupler, a blanking nozzle (17) is hinged to one end of the extruder shell (14), and a quantitative blanking channel (4) is fixed to the feeding port of the extruder shell (14), a mixing blanking hopper (5) is fixed at the top of the quantitative blanking channel (4), a flatness detection device (6) is symmetrically fixed at one end of the translation mechanism (3), and an adjusting and supporting device (7) is fixed at one end of the translation mechanism (3) close to the flatness detection device (6);
the translation mechanism (3) comprises sliding blocks (31), a first cross beam (32), a second cross beam (33), fixing plates (34), a first threaded rod (35), a first motor (36) and a supporting rod (37), the inner wall of the sliding groove (12) is connected with the sliding blocks (31) in a sliding manner, the two ends of each sliding block (31) are symmetrically fixed with the first cross beam (32) and the second cross beam (33), the middle part of each first cross beam (32) is provided with a threaded hole, the inner wall of the translation groove (11) is symmetrically fixed with the fixing plates (34), the middle parts of the two fixing plates (34) are rotatably connected with the first threaded rod (35) through bearings, the first threaded rod (35) is in threaded connection with the middle part of the first cross beam (32), one side of each fixing plate (34) is fixed with the first motor (36), and the output end of the first motor (36) is fixedly connected with the first threaded rod (35), the top of the first cross beam (32) and the top of the second cross beam (33) are symmetrically fixed with support rods (37), and the support rods (37) are fixedly connected with the support base (13).
2. The preparation method of the long-acting antibacterial and mildewproof PP/PS plastic as claimed in claim 1, wherein the quantitative blanking channel (4) comprises a blanking tube (41), a filling block (42), a first rotating shaft (43), a blanking plate (44) and a second motor (45), the blanking tube (41) is fixed at a feeding port of the extruder housing (14), the filling block (42) is symmetrically fixed on the inner wall of the blanking tube (41), the middle part of the filling block (42) is arranged in an arc shape, the first rotating shaft (43) is rotatably connected to the inner wall of the blanking tube (41) through a bearing, the blanking plates (44) are fixed on the outer side of the first rotating shaft (43) at equal intervals, the blanking plates (44) are located in the middle parts of the two filling blocks (42), the end parts of the blanking plate (44) are in sliding contact with the arc-shaped surfaces in the filling block (42), the second motor (45) is fixed on one side of the blanking tube (41), and the output end of the second motor (45) is fixedly connected with the first rotating shaft (43).
3. The preparation method of the long-acting antibacterial and mildewproof PP/PS plastic as claimed in claim 2, wherein the mixing hopper (5) comprises a mixing bin (51), a second rotating shaft (52), a third rotating shaft (53), a second gear (54), a third gear (55), a fourth gear (56), a fifth gear (57), a first mounting plate (58), a third motor (59) and a stirring rod (510), the mixing bin (51) is fixed to the top of the discharging pipe (41), the mixing bin (51) is communicated with the discharging pipe (41), the second rotating shaft (52) is symmetrically and rotatably connected to the upper end of the inner wall of the mixing bin (51) through bearings, the third rotating shaft (53) is rotatably connected to the lower end of the inner wall of the mixing bin (51) through bearings, the second gear (54) is fixed to one end of the second rotating shaft (52) through the mixing bin (51), and the third gear (54) is rotatably connected to one side, close to the second gear (54), of the mixing bin (51), through shaft symmetry 55) The two third gears (55) are respectively meshed with the two second gears (54) and are meshed with each other, the third gears (55) are meshed with each other, a fourth gear (56) is fixed to one end of a third rotating shaft (53), a fifth gear (57) is rotatably connected to one side of the mixing bin (51) through a shaft, the fifth gear (57) is meshed with the fourth gear (56), the fifth gear (57) is meshed with one third gear (55), a first mounting plate (58) is fixed to one side of the mixing bin (51), a third motor (59) is fixed to the top of the first mounting plate (58), the output end of the third motor (59) is fixedly connected with the third rotating shaft (53), and stirring rods (510) are fixed to the outer sides of the second rotating shaft (52) and the third rotating shaft (53) at equal intervals.
4. The preparation method of the long-acting antibacterial and mildewproof PP/PS plastic according to claim 3, wherein the flatness detection device (6) comprises an L-shaped rod (61), a first sliding groove (62), a first sliding block (63), a first sliding rod (64), a first U-shaped plate (65), a first roller (66), a spring (67), a groove (68), a rack (69), a sixth gear (610) and an encoder (611), the L-shaped rod (61) is symmetrically fixed on one side of the second beam (33), the first sliding groove (62) is formed in one end of the L-shaped rod (61), a first through hole is formed in the bottom of the inner wall of the first sliding groove (62), the first sliding block (63) is connected to the inner wall of the first sliding groove (62) in a sliding manner, the first sliding rod (64) is fixed to the bottom of the first sliding rod (64) through the first through hole, and the first U-shaped plate (65) is fixed to the bottom of the first sliding rod (64), first U-shaped board (65) inner wall is connected with first gyro wheel (66) through axle rotation, first spout (62) inner wall is fixed with spring (67), and spring (67) bottom and first slider (63) fixed connection, recess (68) have been seted up to L-shaped board upper end, the second through-hole has been seted up to recess (68) one end, and the second through-hole communicates with first spout (62) and external world respectively, second through-hole inner wall sliding connection has rack (69), and rack (69) and first slider (63) fixed connection, recess (68) inner wall rotates through the bearing and is connected with sixth gear (610), and sixth gear (610) and rack (69) meshing connection, L shape pole (61) one end is fixed with encoder (611), and the input and the middle part fixed connection of sixth gear (610) of encoder (611).
5. The preparation method of the long-acting antibacterial and mildewproof PP/PS plastic according to claim 4, wherein the adjusting and supporting device (7) comprises a U-shaped frame (71), a connecting plate (72), a second threaded rod (73), a sliding plate (74), a second sliding rod (75), a second mounting plate (76), a third mounting plate (77), a second roller (78) and a fourth motor (79), the U-shaped frame (71) is fixed at the bottom of the second cross beam (33), the connecting plate (72) is fixed at the upper end of the inner wall of the U-shaped frame (71), the second threaded rod (73) is symmetrically and rotatably connected with the connecting plate (72) and the inner wall of the U-shaped frame (71) through bearings, the sliding plate (74) is symmetrically and slidably connected with the inner wall of the U-shaped frame (71), threads are arranged in the middle of the sliding plate (74), and the sliding plate (74) is in threaded connection with the second threaded rod (73), slide (74) both ends symmetry is fixed with second slide bar (75), second slide bar (75) pass through slide opening and U-shaped frame (71) sliding connection, two U-shaped frame (71) is passed to second slide bar (75) bottom and is fixed with second mounting panel (76), surface symmetry is fixed with third mounting panel (77) under second mounting panel (76), and two third mounting panel (77) middle parts are connected with second gyro wheel (78) through the rotation of axle, connecting plate (72) top symmetry is fixed with fourth motor (79), and the output and second threaded rod (73) fixed connection of fourth motor (79).
6. The method for preparing the long-acting antibacterial and mildewproof PP/PS plastic according to claim 5, wherein the first roller (66) and the second roller (78) are made of stainless steel, the first roller (66) and the second roller (78) are provided with rubber layers, and the thickness of the rubber layers is 2 mm.
7. The preparation method of the long-acting antibacterial and mildewproof PP/PS plastic as claimed in claim 1, wherein one end of the extruder housing (14) close to the feeding nozzle (17) is hinged with a hydraulic cylinder (18) through a shaft pin, the output end of the hydraulic cylinder (18) is hinged with one end of the feeding nozzle (17) through the shaft pin, and the extruder housing (14) and the feeding nozzle (17) are fixedly connected through a flange.
8. The preparation method of the long-acting antibacterial and mildewproof PP/PS plastic as claimed in claim 1, wherein the fixing legs (2) are arranged in an L shape, and the fixing legs (2) are fixedly connected with the ground through bolts.
9. The method for preparing the long-acting antibacterial and mildewproof PP/PS plastic according to claim 5, wherein the first motor (36), the second motor (45), the third motor (59) and the fourth motor (79) are all speed reduction motors.
10. The long-acting antibacterial mildew-proof PP/PS plastic prepared by the preparation method of any one of claims 1 to 9 is characterized by being prepared from the following raw materials in parts by weight: 120-165 parts of PP (polypropylene) master batch, 240 parts of PS (polystyrene) master batch, 6-13 parts of antibacterial mildew preventive, 6-9 parts of microcrystalline cellulose, 2-4 parts of plasticizer, 1-5 parts of toughening agent, 1-5 parts of antioxidant and 1-3 parts of ultraviolet absorbent.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111003045.0A CN113942136A (en) | 2021-08-30 | 2021-08-30 | Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111003045.0A CN113942136A (en) | 2021-08-30 | 2021-08-30 | Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN113942136A true CN113942136A (en) | 2022-01-18 |
Family
ID=79327550
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202111003045.0A Pending CN113942136A (en) | 2021-08-30 | 2021-08-30 | Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN113942136A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116038933A (en) * | 2023-01-09 | 2023-05-02 | 东莞广丰兴塑胶有限公司 | Preparation process and preparation device of special efficient antibacterial master batch for eva |
Citations (27)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2489945Y (en) * | 2001-07-04 | 2002-05-08 | 南京橡塑机械厂 | Quick plastic separation extruder of extrusion system |
| JP2003127863A (en) * | 2001-10-25 | 2003-05-08 | Daifuku Co Ltd | Carrying truck |
| JP2004129435A (en) * | 2002-10-04 | 2004-04-22 | Sony Corp | Transfer device, control method, and drive mechanism |
| JP2006076229A (en) * | 2004-09-13 | 2006-03-23 | Toshiba Mach Co Ltd | Plasticizing device-attaching method of on-line blend injection molding machine |
| CN201317094Y (en) * | 2008-12-02 | 2009-09-30 | 广东联塑机器制造有限公司 | Screw demounting device for screw extruder |
| US20100252338A1 (en) * | 2009-04-07 | 2010-10-07 | Chunlei Xie | Golf bag vehicle |
| CN205701420U (en) * | 2016-06-08 | 2016-11-23 | 河南工程学院 | The screening of use for laboratory chemical industry powder and batch plant |
| CN107554227A (en) * | 2017-08-14 | 2018-01-09 | 歌尔股份有限公司 | Mobile robot's height adaptive chassis and adaptive approach |
| CN207874800U (en) * | 2018-01-31 | 2018-09-18 | 邢台宏安橡塑机械制造有限公司 | A kind of new type rubber extruder |
| CN108556174A (en) * | 2018-05-22 | 2018-09-21 | 玉环汉新机械科技有限公司 | A kind of injection mold device |
| CN208428626U (en) * | 2018-07-17 | 2019-01-25 | 深圳市海特高分子材料有限公司 | A kind of high molecular material mixing extrusion device |
| CN208746112U (en) * | 2018-07-18 | 2019-04-16 | 山东阿图机器人科技有限公司 | Hang the full landform peddrail mobile robot of tactful adjust automatically |
| JP2019077087A (en) * | 2017-10-24 | 2019-05-23 | 住友ゴム工業株式会社 | Warming extruder, rubber extrusion apparatus and rubber extrusion method |
| CN109820599A (en) * | 2019-03-22 | 2019-05-31 | 重庆金山医疗机器人有限公司 | A kind of driving mechanism and operating table underbody seat for operating table underbody seat |
| CN109895875A (en) * | 2019-03-05 | 2019-06-18 | 齐宽宽 | A kind of handling machinery device with shock-absorbing function for logistics transportation |
| CN110640988A (en) * | 2019-10-09 | 2020-01-03 | 黄石恒盛科技发展有限公司 | Gluing device for roller core rubber coating |
| CN209907170U (en) * | 2019-04-12 | 2020-01-07 | 湖南省湘筑工程有限公司 | Road surface flatness detection device |
| CN210159586U (en) * | 2019-06-11 | 2020-03-20 | 江西远宏实业有限公司 | Modified starch lane feeding system |
| CN111619697A (en) * | 2020-05-11 | 2020-09-04 | 广州百士臣科技有限公司 | Transfer robot with antiskid function |
| CN212242671U (en) * | 2020-07-04 | 2020-12-29 | 东莞市图创智能制造有限公司 | Spray printing equipment |
| CN112500651A (en) * | 2020-11-03 | 2021-03-16 | 台州宽源家居有限公司 | Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof |
| CN112595300A (en) * | 2021-01-03 | 2021-04-02 | 大连识汇岛科技服务有限公司 | Mechanism and method for detecting vertical flatness of constructional engineering |
| CN212989672U (en) * | 2020-07-02 | 2021-04-16 | 武汉驰驭科技有限公司 | Pipeline detection system based on transient electromagnetism |
| CN112715148A (en) * | 2020-06-29 | 2021-04-30 | 潍坊学院 | Corn bract peeling treatment device capable of freely walking in field |
| CN213108104U (en) * | 2020-08-17 | 2021-05-04 | 武汉海派特塑料机械有限公司 | Automatic moving device for machine barrel of conical double-extruder |
| CN112825795A (en) * | 2021-01-13 | 2021-05-25 | 余姚市谐丰模塑有限公司 | Feeding detection system |
| CN112848089A (en) * | 2021-01-08 | 2021-05-28 | 朱建雄 | PVC raw material extrusion device of intermittent type formula ration feeding and even ejection of compact |
-
2021
- 2021-08-30 CN CN202111003045.0A patent/CN113942136A/en active Pending
Patent Citations (27)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2489945Y (en) * | 2001-07-04 | 2002-05-08 | 南京橡塑机械厂 | Quick plastic separation extruder of extrusion system |
| JP2003127863A (en) * | 2001-10-25 | 2003-05-08 | Daifuku Co Ltd | Carrying truck |
| JP2004129435A (en) * | 2002-10-04 | 2004-04-22 | Sony Corp | Transfer device, control method, and drive mechanism |
| JP2006076229A (en) * | 2004-09-13 | 2006-03-23 | Toshiba Mach Co Ltd | Plasticizing device-attaching method of on-line blend injection molding machine |
| CN201317094Y (en) * | 2008-12-02 | 2009-09-30 | 广东联塑机器制造有限公司 | Screw demounting device for screw extruder |
| US20100252338A1 (en) * | 2009-04-07 | 2010-10-07 | Chunlei Xie | Golf bag vehicle |
| CN205701420U (en) * | 2016-06-08 | 2016-11-23 | 河南工程学院 | The screening of use for laboratory chemical industry powder and batch plant |
| CN107554227A (en) * | 2017-08-14 | 2018-01-09 | 歌尔股份有限公司 | Mobile robot's height adaptive chassis and adaptive approach |
| JP2019077087A (en) * | 2017-10-24 | 2019-05-23 | 住友ゴム工業株式会社 | Warming extruder, rubber extrusion apparatus and rubber extrusion method |
| CN207874800U (en) * | 2018-01-31 | 2018-09-18 | 邢台宏安橡塑机械制造有限公司 | A kind of new type rubber extruder |
| CN108556174A (en) * | 2018-05-22 | 2018-09-21 | 玉环汉新机械科技有限公司 | A kind of injection mold device |
| CN208428626U (en) * | 2018-07-17 | 2019-01-25 | 深圳市海特高分子材料有限公司 | A kind of high molecular material mixing extrusion device |
| CN208746112U (en) * | 2018-07-18 | 2019-04-16 | 山东阿图机器人科技有限公司 | Hang the full landform peddrail mobile robot of tactful adjust automatically |
| CN109895875A (en) * | 2019-03-05 | 2019-06-18 | 齐宽宽 | A kind of handling machinery device with shock-absorbing function for logistics transportation |
| CN109820599A (en) * | 2019-03-22 | 2019-05-31 | 重庆金山医疗机器人有限公司 | A kind of driving mechanism and operating table underbody seat for operating table underbody seat |
| CN209907170U (en) * | 2019-04-12 | 2020-01-07 | 湖南省湘筑工程有限公司 | Road surface flatness detection device |
| CN210159586U (en) * | 2019-06-11 | 2020-03-20 | 江西远宏实业有限公司 | Modified starch lane feeding system |
| CN110640988A (en) * | 2019-10-09 | 2020-01-03 | 黄石恒盛科技发展有限公司 | Gluing device for roller core rubber coating |
| CN111619697A (en) * | 2020-05-11 | 2020-09-04 | 广州百士臣科技有限公司 | Transfer robot with antiskid function |
| CN112715148A (en) * | 2020-06-29 | 2021-04-30 | 潍坊学院 | Corn bract peeling treatment device capable of freely walking in field |
| CN212989672U (en) * | 2020-07-02 | 2021-04-16 | 武汉驰驭科技有限公司 | Pipeline detection system based on transient electromagnetism |
| CN212242671U (en) * | 2020-07-04 | 2020-12-29 | 东莞市图创智能制造有限公司 | Spray printing equipment |
| CN213108104U (en) * | 2020-08-17 | 2021-05-04 | 武汉海派特塑料机械有限公司 | Automatic moving device for machine barrel of conical double-extruder |
| CN112500651A (en) * | 2020-11-03 | 2021-03-16 | 台州宽源家居有限公司 | Long-acting antibacterial mildew-proof PP/PS plastic and preparation method thereof |
| CN112595300A (en) * | 2021-01-03 | 2021-04-02 | 大连识汇岛科技服务有限公司 | Mechanism and method for detecting vertical flatness of constructional engineering |
| CN112848089A (en) * | 2021-01-08 | 2021-05-28 | 朱建雄 | PVC raw material extrusion device of intermittent type formula ration feeding and even ejection of compact |
| CN112825795A (en) * | 2021-01-13 | 2021-05-25 | 余姚市谐丰模塑有限公司 | Feeding detection system |
Non-Patent Citations (1)
| Title |
|---|
| 温变英, 中国轻工业出版社 * |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116038933A (en) * | 2023-01-09 | 2023-05-02 | 东莞广丰兴塑胶有限公司 | Preparation process and preparation device of special efficient antibacterial master batch for eva |
| CN116038933B (en) * | 2023-01-09 | 2024-05-17 | 东莞广丰兴塑胶有限公司 | Preparation process and preparation device of special efficient antibacterial master batch for eva |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN107042557B (en) | A kind of Chipboard special efficient rate conditioning device | |
| DE69410846T2 (en) | Extrusion process and plant | |
| CN112171933A (en) | Many material mixing device are used in masterbatch production | |
| CN218906228U (en) | A double-wall corrugated pipe forming machine | |
| CN114917802A (en) | It deposits with flocculating agent ration interpolation equipment to be based on sewage treatment | |
| CN113713654A (en) | Agitating unit is used in production of pyridine dicarboxylic acid | |
| CN107413241A (en) | Composite fertilizer's material homogenizer | |
| CN219171491U (en) | Injection molding machine for pipe fitting machining | |
| CN117719138A (en) | PVC wood-plastic board apparatus for producing | |
| CN106827642A (en) | A kind of software flocculant extrusion formation equipment and its forming method in sewage disposal | |
| CN218077879U (en) | A device for preparing polyhexamethylene biguanide hydrochloride | |
| CN207329804U (en) | A kind of composite fertilizer's material homogenizer for being capable of automatic discharging | |
| CN113021667A (en) | Mixing device for multiple banburying of plasticized rubber and production process thereof | |
| CN215550766U (en) | A extruder feed mechanism for plastic sheet processing | |
| CN207324595U (en) | Composite fertilizer's material homogenizer | |
| KR200377632Y1 (en) | The Extruder-type mixer for a Continuous Mixing of rubber compounding | |
| CN115464830A (en) | Mixed guiding device of polychrome high plasticity liquid silica gel | |
| CN222495319U (en) | A feeding device for an extruder for producing PE pipes | |
| CN221985795U (en) | Double-screw extruder for pure epoxy thermosetting powder coating | |
| CN223701092U (en) | Plastic product drilling equipment | |
| CN219006936U (en) | Extrusion structure for single-screw granulator | |
| CN221249884U (en) | A composite device for wood-plastic composite floor | |
| CN224044252U (en) | Automatic material guiding and turning manipulator under open mill roller | |
| CN221161444U (en) | High-voltage protection mechanism of tractor | |
| CN222093980U (en) | 3-Amino-1-adamantanol screening plant convenient to change filter screen structure |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20220118 |
|
| WD01 | Invention patent application deemed withdrawn after publication |