CN113921309A - A switch automatic assembly machine - Google Patents
A switch automatic assembly machine Download PDFInfo
- Publication number
- CN113921309A CN113921309A CN202111154066.2A CN202111154066A CN113921309A CN 113921309 A CN113921309 A CN 113921309A CN 202111154066 A CN202111154066 A CN 202111154066A CN 113921309 A CN113921309 A CN 113921309A
- Authority
- CN
- China
- Prior art keywords
- plate
- riveting
- assembly
- feeding mechanism
- machine table
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 230000007246 mechanism Effects 0.000 claims abstract description 174
- 238000007599 discharging Methods 0.000 claims abstract description 36
- 239000000463 material Substances 0.000 claims description 109
- 238000005520 cutting process Methods 0.000 claims description 50
- 239000002699 waste material Substances 0.000 claims description 40
- 238000003825 pressing Methods 0.000 claims description 9
- 230000005540 biological transmission Effects 0.000 claims description 8
- 238000000748 compression moulding Methods 0.000 claims 1
- 238000006073 displacement reaction Methods 0.000 claims 1
- 238000000034 method Methods 0.000 abstract description 9
- 230000008569 process Effects 0.000 abstract description 9
- 238000004519 manufacturing process Methods 0.000 abstract description 7
- 230000009471 action Effects 0.000 abstract description 6
- 239000012634 fragment Substances 0.000 description 12
- 230000000712 assembly Effects 0.000 description 5
- 238000000429 assembly Methods 0.000 description 5
- 238000010586 diagram Methods 0.000 description 3
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 description 2
- 230000003139 buffering effect Effects 0.000 description 2
- 230000005012 migration Effects 0.000 description 2
- 238000013508 migration Methods 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 239000000741 silica gel Substances 0.000 description 2
- 229910002027 silica gel Inorganic materials 0.000 description 2
- TVEXGJYMHHTVKP-UHFFFAOYSA-N 6-oxabicyclo[3.2.1]oct-3-en-7-one Chemical compound C1C2C(=O)OC1C=CC2 TVEXGJYMHHTVKP-UHFFFAOYSA-N 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 239000003638 chemical reducing agent Substances 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 230000005484 gravity Effects 0.000 description 1
- 239000013307 optical fiber Substances 0.000 description 1
- 230000003068 static effect Effects 0.000 description 1
Images





Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01H—ELECTRIC SWITCHES; RELAYS; SELECTORS; EMERGENCY PROTECTIVE DEVICES
- H01H11/00—Apparatus or processes specially adapted for the manufacture of electric switches
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Automatic Assembly (AREA)
Abstract
The invention relates to an automatic switch assembling machine which comprises a case, a machine table, a turntable mechanism, an elastic pad loading mechanism, a shell loading mechanism, a base loading mechanism, an elastic sheet loading mechanism, a riveting mechanism and a product discharging mechanism, wherein the machine table, the turntable mechanism, the elastic pad loading mechanism, the shell loading mechanism, the base loading mechanism, the elastic sheet loading mechanism and the riveting mechanism are arranged on the case; the elastic pad feeding mechanism, the shell feeding mechanism, the base feeding mechanism, the elastic piece feeding mechanism and the riveting mechanism are arranged in sequence around the turntable mechanism. The elastic cushion feeding mechanism, the shell feeding mechanism, the base feeding mechanism, the elastic piece feeding mechanism, the riveting mechanism and the product discharging mechanism are arranged around the turntable mechanism, and all product parts of the switch are automatically fed, assembled and discharged, so that the production efficiency is improved, the production cost is reduced, the action consistency in the product assembling process is ensured, the consistency of the product assembling quality is further ensured, and the yield is ensured.
Description
Technical Field
The invention relates to the technical field of switches, in particular to an automatic switch assembling machine.
Background
A switch refers to an electronic component that can open a circuit, interrupt a current, or cause it to flow to other circuits. The microswitch is a kind of switch, and is a kind of switch, which has a minute contact spacing and a quick-acting mechanism, a contact mechanism for performing a switching action with a prescribed stroke and a prescribed force, and a switch covered by a casing and having a driving lever on the outside. Common micro-gap switch generally includes parts such as base, shell fragment, cushion and shell, need assemble into the product to these parts in process of production, in traditional operation mode, mostly the manual work adopts erecting tool or cooperates simple equipment to assemble, and efficiency is lower and intensity of labour is high, and the micro-gap switch of small volume also operates comparatively inconveniently when the assembly, is difficult to guarantee assembly quality.
Disclosure of Invention
In order to solve the problems, the invention provides an automatic switch assembling machine.
The invention is realized by adopting the following scheme:
the utility model provides an automatic kludge of switch for base, shell fragment, cushion and the shell of equipment switch, the automatic kludge of switch includes quick-witted case and sets up the board on quick-witted case, the automatic kludge of switch still includes: the turntable mechanism is arranged on the machine table; the elastic cushion feeding mechanism is used for conveying the elastic cushion to the turntable mechanism; the shell feeding mechanism is used for conveying the shell to the turntable mechanism; the base feeding mechanism is used for conveying a base to the turntable mechanism; the elastic piece feeding mechanism is used for conveying the elastic pieces to the turntable mechanism; the riveting mechanism is used for riveting the base and the shell; the product discharging mechanism is arranged on one side of the riveting mechanism; the elastic pad feeding mechanism, the shell feeding mechanism, the base feeding mechanism, the elastic piece feeding mechanism and the riveting mechanism are arranged in sequence around the turntable mechanism.
Further, the turntable mechanism comprises a divider arranged on the machine table, a rotating disc connected with the divider, a plurality of positioning jigs uniformly arranged on the rotating disc, a lifting plate arranged above the rotating disc, a plurality of carrying assemblies uniformly arranged on the lifting plate, a driving assembly used for driving the divider and the lifting plate, and a transmission assembly used for connecting the driving assembly and the divider; the driving assembly comprises a driving support arranged at the bottom of the machine table, a rotating shaft connected with the driving support, a driving piece used for driving the rotating shaft, and a cam arranged on the rotating shaft, wherein the rotating shaft is connected with the separator through a transmission assembly; and a connecting rod is arranged at the bottom of the lifting plate, and the connecting rod penetrates through the divider and the machine platform to be connected with the cam.
Further, the transport subassembly include movable connection in movable plate on the lifter plate, set up in the fixed block of movable plate one end outwards, set up in product transport piece on the fixed block, and set up in transport cylinder on the movable plate, be provided with a fixed head in the middle of the up end of lifter plate, the output of transport cylinder with the fixed head is connected.
Further, the shell feeding mechanism comprises a material belt conveying assembly arranged on the case, a material cutting assembly arranged on the machine table and a waste material collecting assembly arranged on the machine table; the material cutting assembly comprises a material cutting seat arranged on the machine table, a material cutting support arranged on the material cutting seat, a guide plate arranged on the material cutting support, a first material cutting knife arranged on the guide plate, a second material cutting knife arranged below the guide plate, and a material cutting cylinder arranged on the material cutting seat and used for driving the second material cutting knife to move along the vertical direction.
Further, the waste collecting assembly comprises a waste plate arranged on the machine table, a waste seat arranged on one side of the waste plate, an upper cutter and a lower cutter arranged on the waste seat, and a waste box arranged on the machine table; the upper cutter is movably connected with the waste material seat, and a waste material cylinder used for driving the upper cutter to move along the vertical direction is further arranged at the top of the waste material plate.
Furthermore, the material guide plate is also provided with a material guide assembly, and the material guide assembly comprises a sliding plate movably connected to the material guide plate, a material guide member connected with the sliding plate, and a material guide cylinder for driving the sliding plate to move.
Furthermore, the elastic cushion feeding mechanism and the base feeding mechanism respectively comprise a feeding support arranged on the case, a first vibrating disc arranged on the feeding support, a first feeding channel arranged on the machine table, and a dislocation assembly arranged on the machine table, wherein the dislocation assembly is connected with the end part of the discharging channel; dislocation subassembly including set up in dislocation board on the board, but the portable connection is in the dislocation piece at dislocation board top for the drive the dislocation cylinder that the dislocation piece removed, the dislocation cylinder set up in one side of dislocation board, the output of dislocation cylinder with the dislocation piece is connected.
Further, shell fragment feed mechanism including set up in second vibration dish on the board, set up in shell fragment support on the board sets up in the first horizontal migration module of shell fragment support one side, with the first vertical removal module that first horizontal migration module is connected, with the movable block that first vertical removal module is connected, set up in the shell fragment on the movable block gets the material piece, and set up in shell fragment catch tray on the board, shell fragment catch tray is located the below that the material piece was got to the shell fragment, be provided with the piece of placing that is used for placing the shell fragment on the shell fragment catch tray.
Furthermore, the riveting mechanism comprises a riveting seat arranged on the machine table, a riveting frame arranged on the riveting seat, a riveting plate arranged on the riveting frame, a first sliding block and a second sliding block movably connected to the riveting plate, wherein the first sliding block and the second sliding block are arranged symmetrically at a certain interval, a riveting cylinder is arranged on the riveting seat, the output end of the riveting cylinder is connected with a connecting plate, and a riveting needle and two ejector blocks used for pushing the first sliding block and the second sliding block are arranged on the connecting plate.
Furthermore, the product discharging mechanism comprises a discharging support, a second horizontal moving module arranged on the discharging support, a second vertical moving module connected with the second horizontal moving module, a discharging seat connected with the second vertical moving module, a discharging piece arranged on the discharging seat, and a pressing die assembly arranged on the discharging support and used for pressing the product.
Compared with the prior art, the invention has the following beneficial effects:
1. the elastic cushion feeding mechanism, the shell feeding mechanism, the base feeding mechanism, the elastic piece feeding mechanism, the riveting mechanism and the product discharging mechanism are arranged around the turntable mechanism, and all product parts of the switch are automatically fed, assembled and discharged without manual intervention, so that the production efficiency is improved, and the production cost is reduced.
2. The assembly process of the invention realizes automation, ensures the consistency of the actions of the product assembly process, further ensures the consistency of the product assembly quality and ensures the yield.
3. The carrying assembly can realize the pre-assembly of product parts, and finally, the whole product is riveted and compressed through the matching of the riveting mechanism and the product discharging mechanism, so that the assembly quality of the product is further ensured.
4. The shell feeding mechanism is provided with the material belt conveying assembly, the material cutting assembly and the waste material collecting assembly, so that the shell can be automatically separated from the material belt, and the waste material belt can be automatically cut off and recovered.
Drawings
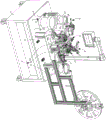
Fig. 1 is a schematic overall structure diagram of an automatic switch assembling machine according to the present invention.
Fig. 2 is a top view of the present invention with the tape transport assembly hidden.
Fig. 3 is a schematic structural diagram of the turntable mechanism of the present invention.
FIG. 4 is a schematic view of another angle of the turntable mechanism of the present invention.
Fig. 5 is a partial structural schematic view of the feeding mechanism of the housing of the present invention, in which the material tape conveying assembly is hidden.
Fig. 6 is a cross-sectional view of the blanking assembly of the present invention.
Fig. 7 is a schematic view of the spring plate loading mechanism of the present invention, in which the second vibration plate and the spring plate collection plate are hidden.
Fig. 8 is a schematic structural diagram of the riveting mechanism of the present invention.
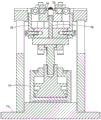
Fig. 9 is a cross-sectional view of the staking mechanism of the present invention.
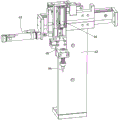
Fig. 10 is a schematic structural view of a product discharge mechanism of the present invention.
FIG. 11 is a schematic view of the malposition assembly of the present invention.
The figure includes:
the machine case 1, the machine table 11, the turntable mechanism 2, the divider 21, the rotating disc 22, the positioning fixture 23, the lifting plate 24, the connecting rod 241, the fixed head 242, the carrying assembly 25, the moving plate 251, the fixed block 252, the product carrying member 253, the carrying cylinder 254, the driving assembly 26, the driving bracket 261, the rotating shaft 262, the driving member 263, the cam 264, the transmission assembly 27, the elastic pad loading mechanism 3, the loading bracket 31, the first vibrating disc 32, the first loading channel 33, the dislocation assembly 34, the dislocation plate 341, the dislocation block 342, the dislocation cylinder 343, the housing loading mechanism 4, the material belt conveying assembly 41, the blanking assembly 42, the blanking seat 421, the blanking bracket 422, the material guiding plate 423, the first blanking knife 424, the second blanking knife 425, the blanking cylinder 426, the waste collecting assembly 43, the waste plate 431, the waste seat 432, the upper blanking knife 433, the lower blanking knife 434, the waste box 435, the waste cylinder 436, the material guiding assembly 44, the positioning assembly, and the product conveying assembly, The device comprises a sliding plate 441, a material guiding piece 442, a material guiding cylinder 443, a base feeding mechanism 5, a spring plate feeding mechanism 6, a second vibrating disk 61, a spring plate support 62, a first horizontal moving module 63, a first vertical moving module 64, a moving block 65, a spring plate material taking piece 66, a spring plate collecting disk 67, a riveting mechanism 7, a riveting seat 71, a riveting frame 72, a riveting plate 73, a first sliding block 74, a second sliding block 75, a riveting cylinder 76, a connecting plate 77, a riveting needle 78, a top block 79, a product discharging mechanism 8, a discharging support 81, a second horizontal moving module 82, a second vertical moving module 83, a discharging seat 84, a discharging piece 85 and a pressing module 86.
Detailed Description
To facilitate an understanding of the present invention for those skilled in the art, the present invention will be described in further detail below with reference to specific embodiments and accompanying drawings.
Referring to fig. 1 to 11, the automatic switch assembling machine provided by the present invention is used for assembling a base, a spring plate, an elastic pad, and a housing of a switch, and includes a case 1 and a machine 11 disposed on the case 1, and further includes: set up carousel mechanism 2, the elastic pad on board 11 and feed mechanism 3, shell feed mechanism 4, base feed mechanism 5, shell fragment feed mechanism 6, riveting mechanism 7, wherein: the elastic pad feeding mechanism 3 is used for conveying the elastic pad to the turntable mechanism 2; a shell feeding mechanism 4 for conveying the shell to the turntable mechanism 2; the base feeding mechanism 5 is used for conveying a base to the turntable mechanism 2; the elastic piece feeding mechanism 6 is used for conveying the elastic pieces to the turntable mechanism 2; the riveting mechanism 7 is used for riveting the base and the shell; and a product discharging mechanism 8 arranged on one side of the riveting mechanism 7.
The elastic pad feeding mechanism 3, the shell feeding mechanism 4, the base feeding mechanism 5, the elastic piece feeding mechanism 6 and the riveting mechanism 7 are sequentially arranged around the turntable mechanism 2 to form an operation cycle. In this embodiment, six operation stations are uniformly arranged on the basis of the center of the turntable mechanism 2, and the area corresponding to the elastic pad loading mechanism 3 is defined as a first operation station, and then the shell loading mechanism 4, the base loading mechanism 5, the elastic sheet loading mechanism 6 and the riveting mechanism 7 are sequentially a second operation station, a third operation station, a fourth operation station, a sixth operation station and a fifth operation station which are combined stations for combining the shell part and the base part, and the riveting mechanism 7 and the product discharging mechanism 8 are located at the sixth station.
The turntable mechanism 2 includes a divider 21 disposed on the machine base 11, a rotating disc 22 connected to the divider 21, a plurality of positioning jigs 23 uniformly disposed on the rotating disc 22, a lifting plate 24 disposed above the rotating disc 22, a plurality of carrying assemblies 25 uniformly disposed on the lifting plate 24, a driving assembly 26 for driving the divider 21 and the lifting plate 24, and a transmission assembly 27 for connecting the driving assembly 26 and the divider 21. In this embodiment, the transmission assembly 27 employs a pulley assembly.
Specifically, two positioning grooves are arranged on the positioning jig 23, one positioning groove is close to the center of the rotating disc 22, and the other positioning groove is far away from the center of the rotating disc 22. in this embodiment, the positioning jig 23 is totally 12, when the rotating disc 22 is static, each carrying assembly 25 corresponds to one positioning jig 23, and at this time, the middle position of each adjacent carrying assembly 25 corresponds to one positioning jig 23. In this embodiment, because 12 positioning jigs 23 are provided, the angle interval between adjacent positioning jigs 23 is 30 °, that is, the angle of each step of rotation of the rotating disc 22 is 30 °, the angle interval between two adjacent carrying assemblies 25 is 60 °, the rotating disc 22 needs to rotate two steps, and the positioning jig 23 at the current carrying assembly 25 is transferred to the downward moving carrying assembly 25. Since the rotary plate 22 and the lifting plate 24 are driven by the driving assembly 26, the carrying assembly 25 can perform lifting movement while the rotary plate 22 rotates.
The driving assembly 26 includes a driving bracket 261 disposed at the bottom of the machine 11, a rotating shaft 262 connected to the driving bracket 261, a driving member 263 for driving the rotating shaft 262, a cam 264 disposed on the rotating shaft 262, the rotating shaft 262 and the separator are connected by a transmission assembly 27, and a speed reducer is further connected between the driving member 263 and the rotating shaft 262. The bottom of the lifting plate 24 is provided with a connecting rod 241, and the connecting rod 241 passes through the divider 21 and the machine platform 11 to be connected with the cam 264. When the rotating shaft 262 rotates, the cam 264 rotates along with the rotating shaft, the connecting rod 241 is driven by the cam 264 to move in the vertical direction, so that the lifting plate 24 is driven to move in the vertical direction, and the carrying mechanism arranged on the lifting plate 24 also moves along with the lifting plate.
The carrying assembly 25 includes a moving plate 251 movably connected to the lifting plate 24, a fixed block 252 disposed at an outward end of the moving plate 251, a product carrying member 253 disposed on the fixed block 252, and a carrying cylinder 254 disposed on the moving plate 251, wherein a fixed head 242 is disposed in the middle of an upper end surface of the lifting plate 24, and an output end of the carrying cylinder 254 is connected to the fixed head 242. In this embodiment, the carrying assembly 25 is provided with six corresponding six working stations, and the number of the positioning jigs 23 is twice that of the carrying assembly 25. A sensor, such as an optical fiber sensor, may be disposed between two adjacent carrying assemblies 25, the sensor is specifically disposed at a middle position of the adjacent carrying assemblies 25, when the rotating disc 22 is stationary, the position of the sensor is aligned to the positioning fixture 23 located at the current position, and at this time, the sensor may detect whether a product component is placed inside the positioning fixture 23. The product carrying part 253 can use a suction nozzle, the specification of the suction nozzle can be adjusted in adaptability according to the current parts to be carried, the suction nozzle capable of being in hard contact (for example, the suction nozzle capable of realizing the pressing function can be adopted at the fifth station) can be adopted, the product carrying part 253 corresponding to the carrying component 25 of the riveting mechanism 7 can adopt a clamping jaw cylinder, and the product can be clamped in the riveting mechanism 7 for riveting. In this embodiment, the lifting plate 24 is circular, the carrying assembly 25 is disposed along a radial direction thereof, when the carrying cylinder 254 is driven, the product carrying member 253 can move in a direction close to or away from the lifting plate 24, when the carrying assembly 25 is away from the lifting plate 24, the product carrying member 253 reaches a corresponding loading position, at this time, the lifting plate 24 moves downward at the same time, the product carrying member 253 takes away the product component, then, the lifting plate 24 resets, the product carrying assembly 25 returns to an initial position, at this time, the lifting plate 24 moves downward, and the product carrying assembly 25 places the product component on the positioning fixture 23.
The shell feeding mechanism 4 includes a material belt conveying assembly 41 disposed on the chassis 1, a material cutting assembly 42 disposed on the machine platform 11, and a waste collecting assembly 43 disposed on the machine platform 11. The material belt conveying assembly 41 specifically comprises a material rack arranged on the chassis 1, a feeding roller arranged on the material rack, and a motor for driving the feeding roller to rotate, and the material belt conveying assembly 41 can convey the material belt of the shell to the material cutting assembly 42.
The material cutting assembly 42 includes a material cutting base 421 disposed on the machine platform 11, a material cutting support 422 disposed on the material cutting base 421, a material guide plate 423 disposed on the material cutting support 422, a first material cutting knife 424 disposed on the material guide plate 423, a second material cutting knife 425 disposed below the material guide plate 423, and a material cutting cylinder 426 disposed on the material cutting base 421 and configured to drive the second material cutting knife 425 to move in a vertical direction. The material guiding plate 423 is provided with a passage for the material belt to pass through, in this embodiment, the first material cutting knife 424 is installed on a knife seat disposed on the material guiding plate 423, the middle of the first material cutting knife 424 is provided with an opening matched with the size of the shell (the corresponding position of the material guiding plate 423 is also provided with an opening), the second material cutting knife 425 is a cylinder, and the cylinder is driven by the material cutting cylinder 426 to move upwards to jack up the material belt, so that the shell enters the opening of the first material cutting knife 424 and is cut off, and the carrying assembly 25 takes away the shell while cutting off. In specific implementation, a guide buffer assembly may be disposed at the bottom of the material guide plate 423, and the output end of the material cutting cylinder 426 is connected to the second material cutting knife 425 through the guide buffer assembly, so that the second material cutting knife 425 operates more stably. The guide buffering assembly can adopt a guide rod and a spring to realize guiding and buffering, meanwhile, a guide sleeve can be sleeved outside the second blanking knife 425, a positioning needle (or a positioning hole) is arranged on the guide sleeve, a positioning hole (or a positioning needle) is arranged on the guide plate 423, and the positioning needle is matched with the positioning hole, so that the second blanking knife 425 runs stably and accurately.
The waste collecting assembly 43 includes a waste plate 431 disposed on the machine platform 11, a waste base 432 disposed on one side of the waste plate 431, an upper cutter 433 and a lower cutter 434 disposed on the waste base 432, and a waste box 435 disposed on the machine platform 11, wherein the upper cutter 433 is movably connected to the waste base 432, and a waste cylinder 436 for driving the upper cutter 433 to move in a vertical direction is further disposed at the top of the waste plate 431. The waste material plate 431 may be provided with an opening through which the material tape passes, and the upper cutter 433 and the lower cutter 434 have an interval corresponding to the above-mentioned opening in an initial state, and the material tape is removed while passing through the cutting assembly 42, and then enters between the upper cutter 433 and the lower cutter 434, and after a certain length of the material tape is extended, the upper cutter 433 and the lower cutter 434 cut the material tape, and the cut portion falls into the waste material box 435 by gravity.
The material guiding assembly 44 is further disposed on the material guiding plate 423, and the material guiding assembly 44 includes a sliding plate 441 movably connected to the material guiding plate 423, a material guiding member 442 connected to the sliding plate 441, and a material guiding cylinder 443 for driving the sliding plate 441 to move. The material belt is preset with a through hole, the material guiding member 442 is provided with a protruding portion capable of being inserted into the through hole, when the cutting assembly 42 cuts, the material belt is lifted, and at this time, the protruding portion can be inserted into the through hole, and the material guiding cylinder 443 drives the sliding plate 441 to move towards the direction of the first cutting blade 424, so that the material belt can be pulled to move a predetermined distance, and the next shell is just aligned with the cutting position of the first cutting blade 424.
Elastic pad feed mechanism 3 with base feed mechanism 5 all including set up in material loading support 31 on quick-witted case 1, set up in first vibration dish 32 on the material loading support 31, set up in first material loading is said 33 on board 11 to and set up dislocation subassembly 34 on board 11, dislocation subassembly 34 with the end connection that the material outlet was said, the below that the material loading was said still is provided with a straight oscillator to guarantee that the part can reach the end that first material loading was said 33. The elastic pad is generally a silica gel pad, and the product carrying piece 253 of the carrying assembly 25 corresponding to the station where the elastic pad loading mechanism 3 is located also adopts a suction nozzle capable of adsorbing the silica gel pad. In specific implementation, a dust removing device can be further arranged on the first feeding channel 33 according to actual requirements.
The dislocation assembly 34 includes a dislocation plate 341 disposed on the machine platform 11, a dislocation block 342 movably connected to the top of the dislocation plate 341, and a dislocation cylinder 343 configured to drive the dislocation block 342 to move, wherein the dislocation cylinder 343 is disposed on one side of the dislocation plate 341, and an output end of the dislocation cylinder 343 is connected to the dislocation block 342. The shift plate 341 has a groove for placing a product component, and after the product component enters the groove from the first feeding path 33, the shift cylinder 343 drives the shift block 342 to move, so that the product component moves to a position corresponding to the product carrier 253. The indexing assembly 34 may act as a stop for the material to ensure that the product components are loaded in order.
The elastic sheet feeding mechanism 6 comprises a second vibration disc 61 arranged on the machine table 11, an elastic sheet support 62 arranged on the machine table 11, a first horizontal moving module 63 arranged on one side of the elastic sheet support 62, a first vertical moving module 64 connected with the first horizontal moving module 63, a moving block 65 connected with the first vertical moving module 64, an elastic sheet taking piece 66 arranged on the moving block 65, and an elastic sheet collecting disc 67 arranged on the machine table 11, wherein the elastic sheet collecting disc 67 is located below the elastic sheet taking piece 66, a placing piece used for placing the elastic sheet is arranged on the elastic sheet collecting disc 67, the placing piece is provided with two pieces, one piece is close to the turntable mechanism 2, the other piece is close to the second vibration disc 61, and the elastic sheet taking piece 66 can carry the elastic sheet to the placing piece close to the second vibration disc 61. The placing piece is a cylinder substantially, a lower concave part used for placing the elastic sheet is arranged at the top end of the placing piece, and the placing piece can be used for placing the elastic sheet in advance, so that the position and orientation of the elastic sheet are ensured, and the carrying assembly 25 is convenient to accurately place the elastic sheet to the corresponding position of the base. The carrying assembly 25 corresponding to the elastic sheet feeding mechanism 6 is provided with two product carrying pieces 253 which correspond to the two placing pieces respectively, and in the process of carrying the elastic sheets in the placing pieces close to the turntable mechanism 2 to the jig, the elastic sheets in the placing pieces far away from one side of the turntable mechanism 2 can be carried to the placing pieces close to the turntable mechanism 2. In this embodiment, the first horizontal moving module 63 and the second horizontal moving module 82 both use an air cylinder and a slider rail, and the slider rail is driven to move by the air cylinder.
The riveting mechanism 7 comprises a riveting seat 71 arranged on the machine platform 11, a riveting frame 72 arranged on the riveting seat 71, a riveting plate 73 arranged on the riveting frame 72, a first slider 74 and a second slider 75 movably connected to the riveting plate 73, wherein the first slider 74 and the second slider 75 are arranged symmetrically at a certain interval, a riveting cylinder 76 is arranged on the riveting seat 71, the output end of the riveting cylinder 76 is connected with a connecting plate 77, a riveting needle 78 is arranged on the connecting plate 77, and two top blocks 79 for pushing the first slider 74 and the second slider 75 are arranged. The rivet plate 73 is pre-provided with a slide groove for accommodating the first slider 74 and the second slider 75, and a groove for placing a product. Taking the top block 79 on one side of the first slider 74 as an example, one side of the top block 79 facing the first slider 74 has an inclined surface, and after the top block 79 moves upwards, the inclined surface contacts with the end of the first slider 74 to push the first slider 74 to move towards the product, and the same is true for the second slider 75. The two sides of the shell are provided with connecting arms, the first sliding block 74 and the second sliding block 75 move oppositely, and meanwhile, pressure is applied to the shell of a product placed in the middle position, so that the two connecting arms can be pre-folded, and the riveting needle below is upwards pushed to rivet the shell and the base.
The product discharging mechanism 8 comprises a discharging support 81, a second horizontal moving module 82 arranged on the discharging support 81, a second vertical moving module 83 connected with the second horizontal moving module 82, a discharging seat 84 connected with the second vertical moving module 83, a discharging part 85 arranged on the discharging seat 84, and a pressing die assembly 86 arranged on the discharging support 81 and used for pressing a product, wherein the discharging part 85 can adopt a suction nozzle capable of being in hard contact with the suction nozzle. In this embodiment, the second horizontal moving module 82 and the second vertical moving module 83 both use an air cylinder and a slider rail, and the air cylinder drives the slider rail to move. In specific implementation, other mechanisms capable of realizing the linear movement function, such as a lead screw, may be used. The die assembly 86 specifically includes a fixed block 252 disposed on the discharging bracket 81, a die block movably connected to the fixed block 252, and a die cylinder for driving the die block to move. The first vertical moving mechanism adopts a mode that the sliding block is fixed and the guide rail moves, the tail end of the guide rail extends upwards for a certain length, when the discharging piece 85 reaches the riveting mechanism 7 and moves downwards to be in contact with a product, the pressing module moves to the upper end of the guide rail and is in contact with the guide rail, the material taking piece is ensured to have certain downward pressure, and therefore the material taking piece can be matched with the riveting needle 78 of the riveting mechanism 7 one by one to realize final riveting action of the product.
When the elastic cushion feeding mechanism 3 is used for assembling, firstly, the elastic cushion is conveyed to a preset position by the elastic cushion feeding mechanism 3, the corresponding conveying assembly 25 takes away the elastic cushion and places the elastic cushion in the positioning groove of the positioning jig 23 far away from the center of the rotating disc 22, the rotating disc 22 rotates one step, the corresponding sensor detects whether the elastic cushion is placed in place or not, the rotating disc 22 continues to rotate one step, the positioning jig 23 reaches the shell feeding mechanism 4, the conveying assembly 25 simultaneously conveys the shell to the upper part of the elastic cushion, and the shell is sleeved on the elastic cushion. The turn disc 22 continues to rotate one step and the corresponding sensor detects whether the housing is in place. The base feeding mechanism 5 conveys the base to a preset position, the rotating disc 22 continues to rotate one step, and the conveying assembly 25 at the corresponding position conveys the base to the positioning groove of the positioning jig 23 close to the center of the rotating disc 22. The turn disc 22 continues to rotate one step and the corresponding sensor detects whether the base is in place. The elastic sheet feeding mechanism 6 conveys the elastic sheet to the placing piece, the turntable continues to rotate one step, and the conveying assembly 25 conveys the elastic sheet to the position above the base. The rotating disc 22 continues to rotate one step, no operation is performed at this position (at this time, the above operations and the circulation operations are repeated at other stations of the rotating disc 22), the rotating disc 22 continues to rotate one step, and the carrying assembly 25 carries the combination of the shell and the elastic pad to the upper side of the base and the elastic sheet for preliminary pressing. The rotating disc 22 continues to rotate one step, the position is not operated, the rotating disc 22 continues to rotate one step, the carrying assembly 25 at the corresponding position carries the product assembly to the riveting mechanism 7, the riveting mechanism 7 carries out final riveting on the product assembly, and after riveting is finished, the product discharging mechanism 8 takes out the assembled product from the riveting mechanism 7 and places the assembled product in a finished product box or a conveyor belt to be conveyed away. The above working process is described by taking an action process experienced during the rotation of one of the positioning jigs 23 as an example, and when the positioning jig 23 performs the assembling operation in cooperation with the mechanism or component at the current position, the other positioning jigs 23 also perform the corresponding assembling operation in cooperation with the other mechanisms at the current position.
The elastic cushion feeding mechanism 3, the shell feeding mechanism 4, the base feeding mechanism 5, the elastic piece feeding mechanism 6, the riveting mechanism 7 and the product discharging mechanism 8 are arranged around the turntable mechanism 2, and all product parts of the switch are automatically fed, assembled and discharged without manual intervention, so that the production efficiency is improved, and the production cost is reduced. The assembly process of the invention realizes automation, ensures the consistency of the actions of the product assembly process, further ensures the consistency of the product assembly quality and ensures the yield. The carrying assembly 25 can pre-assemble product components, and finally, the whole product is riveted and compressed through the matching of the riveting mechanism 7 and the product discharging mechanism 8, so that the assembly quality of the product is further ensured. The shell feeding mechanism 4 is provided with a material belt conveying assembly 41, a material cutting assembly 42 and a waste material collecting assembly 43, so that the shell can be automatically separated from the material belt, and the waste material belt can be automatically cut off and recovered.
In the description of the present invention, it is to be understood that the indicated orientations or positional relationships are based on the orientations or positional relationships shown in the drawings and are only for convenience in describing the present invention and simplifying the description, but are not intended to indicate or imply that the indicated devices or elements must have a particular orientation, be constructed and operated in a particular orientation, and are not to be construed as limiting the present invention.
Furthermore, the terms "first", "second", etc. are used for descriptive purposes only and are not to be construed as indicating or implying relative importance or implicitly indicating the number of technical features indicated. Thus, a feature defined as "first" or "second" may explicitly or implicitly include one or more of that feature. In the description of the present invention, "a plurality" means two or more unless specifically defined otherwise.
In the present invention, unless otherwise expressly stated or limited, the terms "connected," "secured," and the like are to be construed broadly, e.g., as meaning permanently attached, removably attached, or integral to one another; can be mechanically or electrically connected; either directly or indirectly through intervening media, either internally or in any other relationship. The specific meanings of the above terms in the present invention can be understood by those skilled in the art according to specific situations.
While the invention has been described in conjunction with the specific embodiments set forth above, it is evident that many alternatives, modifications, and variations will be apparent to those skilled in the art in light of the foregoing description. Accordingly, it is intended to embrace all such alternatives, modifications, and variations that fall within the scope of the included claims.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111154066.2A CN113921309B (en) | 2021-09-29 | 2021-09-29 | Automatic switch assembly machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111154066.2A CN113921309B (en) | 2021-09-29 | 2021-09-29 | Automatic switch assembly machine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN113921309A true CN113921309A (en) | 2022-01-11 |
| CN113921309B CN113921309B (en) | 2024-11-05 |
Family
ID=79237059
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202111154066.2A Active CN113921309B (en) | 2021-09-29 | 2021-09-29 | Automatic switch assembly machine |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN113921309B (en) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114464478A (en) * | 2022-02-17 | 2022-05-10 | 东莞市万将机电设备有限公司 | Turntable device in automatic assembling machine for microswitch |
| CN114496620A (en) * | 2022-02-17 | 2022-05-13 | 东莞市万将机电设备有限公司 | Automatic kludge of micro-gap switch |
| CN116673425A (en) * | 2022-02-22 | 2023-09-01 | 明门(中国)幼童用品有限公司 | Rivet system |
| CN117921337A (en) * | 2024-02-05 | 2024-04-26 | 维益宏基(浙江)电力股份有限公司 | Full-automatic flexible production system for elastic lock catch of high-voltage switch cabinet |
| DE102023001887A1 (en) * | 2023-05-10 | 2024-11-14 | Fritz Stepper GmbH & Co. KG. | Assembly device for assembling at least two components |
| CN121179020A (en) * | 2025-11-25 | 2025-12-23 | 深圳市精而美科技有限公司 | A charging terminal assembly device inside the bottom shell of a wearable product terminal |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101673630A (en) * | 2009-10-12 | 2010-03-17 | 温州和泰电子有限公司 | Automatic assembling machine of light touch switch |
| CN101697329A (en) * | 2009-10-12 | 2010-04-21 | 温州和泰电子有限公司 | Slight-touch switch upper cover and button assembly charging indexing device |
| CN101777448A (en) * | 2009-12-31 | 2010-07-14 | 惠州市利元亨精密自动化有限公司 | Automatic assembly machine for touch switch |
| CN201853608U (en) * | 2010-06-01 | 2011-06-01 | 东莞市焦点自动化科技有限公司 | Tact switch automatic assembly machine |
| CN105655170A (en) * | 2016-04-14 | 2016-06-08 | 深圳市鸿源精密器材有限公司 | Automatic assembling machine of touch switch |
| CN105845476A (en) * | 2016-05-20 | 2016-08-10 | 东莞市鼎力自动化科技有限公司 | A small micro switch automatic assembly machine |
| CN107322296A (en) * | 2017-08-15 | 2017-11-07 | 宁波永佳电子科技有限公司 | A kind of code switch Full-automatic assembling machine |
| CN109390174A (en) * | 2018-12-29 | 2019-02-26 | 深圳市鸿源精密器材有限公司 | Press the automatic assembling of touch-switch in a kind of three-layer type side |
| CN212303482U (en) * | 2020-09-01 | 2021-01-05 | 深圳市鸿源精密器材有限公司 | Single-layer tact switch automatic assembly machine |
| CN212750659U (en) * | 2020-08-17 | 2021-03-19 | 惠州市瑞度电子有限公司 | Contact equipment is riveted to shell fragment |
-
2021
- 2021-09-29 CN CN202111154066.2A patent/CN113921309B/en active Active
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101673630A (en) * | 2009-10-12 | 2010-03-17 | 温州和泰电子有限公司 | Automatic assembling machine of light touch switch |
| CN101697329A (en) * | 2009-10-12 | 2010-04-21 | 温州和泰电子有限公司 | Slight-touch switch upper cover and button assembly charging indexing device |
| CN101777448A (en) * | 2009-12-31 | 2010-07-14 | 惠州市利元亨精密自动化有限公司 | Automatic assembly machine for touch switch |
| CN201853608U (en) * | 2010-06-01 | 2011-06-01 | 东莞市焦点自动化科技有限公司 | Tact switch automatic assembly machine |
| CN105655170A (en) * | 2016-04-14 | 2016-06-08 | 深圳市鸿源精密器材有限公司 | Automatic assembling machine of touch switch |
| CN105845476A (en) * | 2016-05-20 | 2016-08-10 | 东莞市鼎力自动化科技有限公司 | A small micro switch automatic assembly machine |
| CN107322296A (en) * | 2017-08-15 | 2017-11-07 | 宁波永佳电子科技有限公司 | A kind of code switch Full-automatic assembling machine |
| CN109390174A (en) * | 2018-12-29 | 2019-02-26 | 深圳市鸿源精密器材有限公司 | Press the automatic assembling of touch-switch in a kind of three-layer type side |
| CN212750659U (en) * | 2020-08-17 | 2021-03-19 | 惠州市瑞度电子有限公司 | Contact equipment is riveted to shell fragment |
| CN212303482U (en) * | 2020-09-01 | 2021-01-05 | 深圳市鸿源精密器材有限公司 | Single-layer tact switch automatic assembly machine |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114464478A (en) * | 2022-02-17 | 2022-05-10 | 东莞市万将机电设备有限公司 | Turntable device in automatic assembling machine for microswitch |
| CN114496620A (en) * | 2022-02-17 | 2022-05-13 | 东莞市万将机电设备有限公司 | Automatic kludge of micro-gap switch |
| CN114496620B (en) * | 2022-02-17 | 2024-02-23 | 东莞市万将机电设备有限公司 | Automatic micro-gap switch kludge |
| CN114464478B (en) * | 2022-02-17 | 2024-04-09 | 东莞市万将机电设备有限公司 | Turntable device in automatic microswitch assembling machine |
| CN116673425A (en) * | 2022-02-22 | 2023-09-01 | 明门(中国)幼童用品有限公司 | Rivet system |
| CN116673425B (en) * | 2022-02-22 | 2025-12-23 | 明门(中国)幼童用品有限公司 | Riveting system |
| DE102023001887A1 (en) * | 2023-05-10 | 2024-11-14 | Fritz Stepper GmbH & Co. KG. | Assembly device for assembling at least two components |
| CN117921337A (en) * | 2024-02-05 | 2024-04-26 | 维益宏基(浙江)电力股份有限公司 | Full-automatic flexible production system for elastic lock catch of high-voltage switch cabinet |
| CN121179020A (en) * | 2025-11-25 | 2025-12-23 | 深圳市精而美科技有限公司 | A charging terminal assembly device inside the bottom shell of a wearable product terminal |
Also Published As
| Publication number | Publication date |
|---|---|
| CN113921309B (en) | 2024-11-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN113921309B (en) | Automatic switch assembly machine | |
| CN109950774B (en) | DC socket processing equipment | |
| CN107170606B (en) | Shrapnel type waterproof switch automatic assembly machine | |
| CN210451737U (en) | Sliding potentiometer assembling equipment | |
| CN114472213A (en) | Fan blade equipment and performance detection integrated equipment of motor | |
| CN209140284U (en) | A fully automatic assembly equipment for pressing rotary encoder for multimedia | |
| CN113732696A (en) | Shell of power adapter and conductive elastic sheet automatic feeding kludge | |
| CN217342387U (en) | Fan blade equipment and performance detection integrated equipment of motor | |
| CN215357174U (en) | Temperature controller assembling machine | |
| CN112828951B (en) | Automatic processing device | |
| CN214816414U (en) | Filter core shell lower cover automatic assembly machine | |
| CN207097973U (en) | A kind of battery core switching chip bonding machine | |
| CN113696140A (en) | Torsional spring assembly machine | |
| CN115609935B (en) | Light guide column assembly equipment capable of automatically separating light guide column and water gap | |
| CN219968125U (en) | Automatic change cutting device | |
| CN209867901U (en) | Automatic lamp tail assembling machine | |
| CN215363525U (en) | Feeding device of temperature controller bottom shell assembly | |
| CN216189017U (en) | Elastic sheet assembling device | |
| CN213165796U (en) | Hollow encoder assembling equipment | |
| CN114505598A (en) | Multistation neodymium iron boron cutting device | |
| CN212288829U (en) | Automatic rubber ring sleeving equipment | |
| CN216503370U (en) | Assembling and riveting machine for bypass valve of oil filter | |
| CN209615730U (en) | A plate folding mechanism and an automatic plate splitting machine with the plate folding mechanism | |
| CN222269165U (en) | A circuit board batch welding device | |
| CN108581502B (en) | Special buckle automatic processing device of integrated wallboard |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |