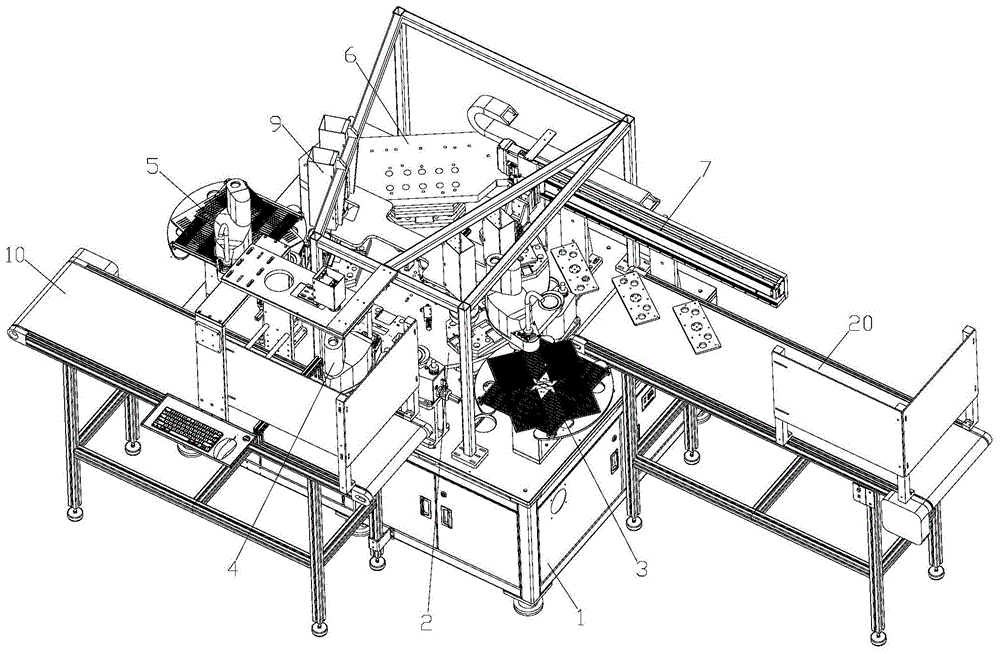
Keyboard riveting machine
Technical Field
The invention relates to the field of riveting mechanical equipment, in particular to a keyboard riveting machine.
Background
With the continuous improvement of the industrial automation degree, the manufacturing industry gradually realizes intellectualization and unmanned; especially for keyboard workpieces, a plurality of processes cannot be automated, and the degree of mechanization determines the overall production efficiency.
The main parts of the keyboard comprise a main board, and the main board is generally connected with other parts through nuts and studs at present, so that the subsequent assembly can be conveniently realized only by riveting the nuts, the studs and other workpieces on the main board. However, in the existing production and manufacturing process, the process is still manually performed, mainly because: the nut, the stud and other workpieces are bulk materials and have small sizes. The existing manual nut and stud riveting is low in production efficiency, four nuts are riveted to the front side of a main board of a common keyboard, two studs are riveted to the back side of the main board, a riveting production line can be completed only by at least 10 persons through cooperation, and the labor input cost is high.
Disclosure of Invention
The invention aims to provide a keyboard riveting machine which can solve at least one of the problems.
According to one aspect of the invention, a keyboard riveting machine is provided, which comprises a machine body, a turntable device, a first material sucking and conveying device, a second material sucking and conveying device, a third material sucking and conveying device, a riveting device and a blanking device, wherein the turntable device, the first material sucking and conveying device, the second material sucking and conveying device, the third material sucking and conveying device, the riveting device and the blanking device are arranged on the machine body;
the turntable device comprises a rotating disc and a plurality of positioning jigs arranged on the edge of the rotating disc along the central circumference array of the rotating disc;
the first material sucking and conveying device, the second material sucking and conveying device, the third material sucking and conveying device, the riveting device and the blanking device are sequentially arranged on the periphery of the rotating disc along the clockwise rotating direction of the rotating disc;
the first material sucking and conveying device is configured to suck the studs and convey the studs to the positioning jig of the rotating disc;
the second material sucking and conveying device is configured to suck the keyboard workpiece and convey the keyboard workpiece to the positioning jig of the rotating disc, so that the keyboard workpiece covers the upper part of the stud;
the third material sucking and conveying device is configured to suck the nuts and convey the nuts to the keyboard workpiece on the positioning jig;
the riveting device is configured to rivet the nut to the keyboard workpiece;
the blanking device is configured to output the product after riveting.
Therefore, the invention provides a keyboard riveting machine with a brand-new structure, and the working principle of the keyboard riveting machine is as follows:
a. the first material sucking and conveying device sucks the stud and puts the stud on a positioning jig of the rotating disc;
b. the rotating disc rotates to drive the positioning jig containing the studs to move to the rear of the second material suction conveying device, and the second material suction conveying device sucks the keyboard workpiece and puts the keyboard workpiece into the positioning jig, so that the keyboard workpiece falls above the studs;
c. the rotating disc continues to rotate to drive the positioning jig containing the stud and the keyboard workpiece to move to the rear of the third material suction conveying device, and the third material suction conveying device sucks the nut and places the nut on the keyboard workpiece;
d. the rotating disc continues to rotate, so that the positioning jig rotates to the riveting station, and the riveting device rivets the nut on the keyboard workpiece;
e. the rotating disc continues to rotate to the blanking station, and the blanking device takes materials from the positioning jig and outputs the materials.
Therefore, the keyboard riveting machine provided by the invention realizes automation of loading, unloading, detection and riveting, facilitates automatic production of the keyboard, can improve the utilization rate, can reduce the manpower input and saves the cost.
In some embodiments, the first suction conveying device comprises a first suction mechanism and a multi-shaft driving mechanism, the multi-shaft driving mechanism is mounted on the machine body, and the first suction mechanism is mounted on the multi-shaft driving mechanism;
first material suction mechanism includes first mounting bracket and installs a plurality ofly and double-screw bolt matched with on first mounting bracket inhale the material subassembly.
In some embodiments, the first suction conveying device further comprises a turntable changing mechanism, the turntable changing mechanism is mounted on the machine body and located on the periphery of the rotating disc, the turntable changing mechanism is used for containing a first material disc bearing the stud, and the turntable changing mechanism comprises a turntable and a plurality of limiting blocks arranged on the turntable and in limiting fit with the first material disc.
In some embodiments, the multi-axis drive mechanism is a four-axis robot.
In some embodiments, the keyboard riveting machine further comprises a pressing device, the pressing device comprises a second mounting frame, a first driving piece and a pressing plate, the second mounting frame is mounted on the machine body and located on the periphery of the rotating disc, the first driving piece is mounted on the second mounting frame, and the pressing plate is mounted at the driving end of the first driving piece and matched with the positioning jig. Therefore, under the driving of the first driving piece, the pressing plate can press and place the keyboard workpiece in the positioning jig downwards, so that the stud is pressed in the keyboard workpiece.
In some embodiments, the keyboard riveting machine further includes a vision detection device, the vision detection device includes a third mounting bracket, a first detection mechanism and a second detection mechanism, the third mounting bracket is mounted on the machine body and erected on the periphery of the rotating disc, the first detection mechanism is mounted on the inner side of the first material suction conveying device and located above the positioning jig, the second detection mechanism is mounted on the inner side of the third material suction conveying device and located above the positioning jig, and the first detection mechanism and the second detection mechanism are a CCD vision detection module. Therefore, the first detection mechanism can identify the stud input by the first suction conveying device and feed back the corresponding position information to the control device, and the second detection mechanism can identify the nut input by the third suction conveying device and feed back the corresponding position information to the control device, so that the feeding and discharging are accurate, and the production efficiency is improved.
In some embodiments, the turntable device is of a turntable structure, the turntable device further includes a driving module for driving the turntable to rotate, the driving module is disposed below the turntable and is in power connection with the turntable, and the positioning fixture is provided with a first limiting groove matched with the stud and a second limiting groove matched with the keyboard workpiece.
In some embodiments, the turntable device further comprises a positioning mechanism, the positioning mechanism is a movable positioning jig which can be lifted relative to the rotating disc, the positioning mechanism is mounted on the machine body and is positioned at the bottom of the rotating disc, and the positioning mechanism is matched with the positioning jig and used for limiting the positioning jig;
the positioning jig comprises an upper module, a lower module and guide posts, wherein the upper module is arranged above the rotating disc, the lower module is arranged below the rotating disc, the upper module and the lower module are connected through the guide posts, and the guide posts penetrate through the rotating disc;
the positioning mechanism comprises a second driving piece and a positioning piece, the second driving piece is installed on the machine body, and the positioning piece is installed at the driving end of the second driving piece and is in limit fit with the lower module.
Therefore, the positioning mechanism can position and support the positioning jig and assist other devices to finish corresponding operation.
In some embodiments, the riveting device includes a fourth mounting frame and a riveting mechanism installed on the fourth mounting frame, the riveting mechanism includes a third driving part and a riveting upper die, the riveting upper die is installed on the fourth mounting frame and located above the upper module of the positioning jig, the third driving part is installed on the machine body and located below the lower module of the positioning jig, the fourth mounting frame includes an upper frame body, a lower frame body and an upper connection frame body, a connection block of the lower frame body, a cavity for accommodating the riveting upper die, the positioning jig and a containing cavity capable of enabling the rotating disc to move therein is formed between the upper frame body and the lower frame body, the riveting upper die is fixedly installed on the upper frame body and located above the positioning jig, and the upper end of the third driving part is fixed at the bottom of the lower frame body and the driving end of the third driving part can lift up the positioning jig. Therefore, when the positioning jig rotates to the riveting station, the riveting mechanism works, the third driving piece upwards jacks the positioning jig, so that the whole positioning jig rises, the upper module is close to the riveting upper die to complete die assembly, and riveting of the nut and the keyboard workpiece is completed.
In some embodiments, the blanking device comprises a single-shaft driving mechanism, a rotating mechanism and a second material sucking mechanism, wherein the single-shaft driving mechanism is installed on the machine body, the rotating mechanism is installed on the single-shaft driving mechanism, and the second material sucking mechanism is installed on the rotating mechanism and matched with the keyboard workpiece in the positioning jig.
In some embodiments, the keyboard riveting machine further comprises a feeding device and a discharging device, the feeding device and the discharging device are arranged on the side of the machine body, the tail end of the feeding device is located in front of the second material suction conveying device, and the front end of the discharging device is located at the discharging tail end of the discharging device.
The invention has the beneficial effects that:
the keyboard riveting machine provided by the invention realizes automation of feeding, discharging, detecting and riveting, is convenient for realizing automatic production of the keyboard, can improve the utilization rate, can reduce the labor input and saves the cost.
Drawings
Fig. 1 is a schematic perspective view of a keyboard riveting machine according to an embodiment of the invention;
FIG. 2 is a schematic top view of the keyboard riveter shown in FIG. 1;
fig. 3 is a schematic perspective view of the keyboard riveting machine shown in fig. 1 with a part of the structure omitted;
fig. 4 is a schematic perspective view of a first material sucking and conveying device of the keyboard riveting machine shown in fig. 1;
fig. 5 is a schematic perspective view of a first material sucking and conveying device of the keyboard riveting machine shown in fig. 1;
fig. 6 is a schematic perspective view of a turntable device of the keyboard riveting machine shown in fig. 1;
FIG. 7 is a schematic perspective view of the positioning fixture and the positioning mechanism of the turntable device shown in FIG. 6;
fig. 8 is a schematic perspective view of a visual inspection device of the keyboard riveting machine shown in fig. 1;
fig. 9 is a schematic perspective view of a pressing device of the keyboard riveting machine shown in fig. 8;
fig. 10 is one of schematic perspective views of a riveting device of the keyboard riveting machine shown in fig. 1;
fig. 11 is a second schematic perspective view of a riveting device of the keyboard riveting machine shown in fig. 1;
fig. 12 is a schematic perspective view of a blanking device of the keyboard riveting machine shown in fig. 1.
Reference numerals in FIGS. 1 to 12: 1-body; 2-a turntable device; 3-a first suction conveyor; 4-a second material sucking and conveying device; 5-a third material sucking and conveying device; 6-riveting means; 7-a blanking device; 8-a pressing device; 9-a visual inspection device; 10-a feeding device; 20-a discharging device; 21-a rotating disc; 22-positioning a jig; 23-a drive module; 24-a positioning mechanism; 31-a first suction mechanism; 32-a multi-axis drive mechanism; 33-a turntable changer mechanism; 61-a fourth mounting frame; 62-a riveting mechanism; 71-single axis drive mechanism; 72-a rotation mechanism; 73-a second material suction mechanism; 81-a second mount; 82-a first drive member; 83-a pressure plate; 91-a third mounting frame; 92-a first detection mechanism; 93-a second detection mechanism; 100-keyboard workpieces; 200-a first tray; 300-a second tray; 221-an upper module; 222-a lower module; 223-a guide post; 241-a second driving member; 242-positioning block; 311-a first mounting frame; 312-a suction assembly; 331-a turntable; 332-a stop block; 611-upper frame body; 612-lower rack body; 613-connecting block; 620-a containment chamber; 621-a third driver; 622-riveting the upper die; 242 a-locating projection.
Detailed Description
The present invention will be described in further detail with reference to the accompanying drawings.
FIGS. 1-12 schematically illustrate a keyboard riveter according to one embodiment of the present invention.
As shown in fig. 1 to 12, the keyboard riveting machine includes a machine body 1, and a turntable device 2, a first material suction conveying device 3, a second material suction conveying device 4, a third material suction conveying device 5, a pressing device 8, a riveting device 6 and a blanking device 7 which are arranged on the machine body 1.
The turntable device 2 comprises a rotating disc 21 and a plurality of positioning jigs 22 arranged on the edge of the rotating disc 21 along the central circumference array of the rotating disc 21;
the first material sucking and conveying device 3, the second material sucking and conveying device 4, the third material sucking and conveying device 5, the riveting device 6 and the blanking device 7 are sequentially arranged on the periphery of the rotating disc 21 along the clockwise rotating direction of the rotating disc 21;
the first suction conveying device 3 is configured to suck the studs and convey the studs onto the positioning jig 22 of the rotary disc 21;
the second material sucking and conveying device 4 is configured to suck the keyboard workpiece 100 and convey the keyboard workpiece 100 onto the positioning jig 22 of the rotary disc 21, so that the keyboard workpiece 100 covers the upper part of the stud;
the third material sucking and conveying device 5 is configured to suck the nuts and convey the nuts to the keyboard workpiece 100 on the positioning jig 22;
the riveting device 6 is configured to rivet a nut to the keyboard workpiece 100;
the blanking device 7 is configured to output the product after the riveting is completed.
As shown in fig. 4, the first suction conveyer 3 includes a first suction mechanism 31 and a multi-axis driving mechanism 32, the multi-axis driving mechanism 32 is mounted on the machine body 1, and the first suction mechanism 31 is mounted on the multi-axis driving mechanism 32;
the first material suction mechanism 31 includes a first mounting bracket 311 and a plurality of material suction components 312 mounted on the first mounting bracket 311 and matched with the studs, and the material suction components 312 are composed of a vacuum generator, a vacuum chuck and the like.
The multi-axis driving mechanism 32 of the present embodiment may be a four-axis robot, specifically, a SCARA robot.
The first material sucking and conveying device 3 further comprises a rotary disc changing mechanism 33, the rotary disc changing mechanism 33 is installed on the machine body 1 and located on the periphery of the rotary disc 21, the rotary disc changing mechanism 33 is used for containing a first material disc 200 bearing a stud, and the rotary disc changing mechanism 33 comprises a rotary disc 331 and a plurality of limiting blocks 332 which are arranged on the rotary disc 331 and are in limiting fit with the first material disc 200. The turntable 331 is driven by a rotary motor.
The third material sucking and conveying device 5 of the present embodiment has basically the same structure as the first material sucking and conveying device 3, and is different only in that the structure of the suction cup of the first material sucking mechanism 31 is different, and the rotary disc changing mechanism 33 is used for accommodating the second material disc 300 carrying the nut; similarly, the structure of the second suction conveyer 4 is substantially the same as that of the first suction conveyer 3, and the second suction conveyer includes a first suction mechanism 31 and a multi-axis driving mechanism 32, and the multi-axis driving mechanism 32 is also a four-axis robot.
As shown in fig. 8 and 9, the keyboard riveting machine of the present embodiment further includes a pressing device 8. The pressing device 8 includes a second mounting bracket 81, a first driving member 82, and a pressing plate 83. The second mounting bracket 81 is mounted on the machine body 1 and located at the periphery of the rotating disc 21, the first driving member 82 is mounted on the second mounting bracket 81, and the pressing plate 83 is mounted at the driving end of the first driving member 82 and is matched with the positioning jig 22. The first driving member 82 of the present embodiment may be a telescopic cylinder. Thus, under the driving of the first driving member 82, the pressing plate 83 can press the keyboard workpiece 100 in the positioning fixture 22 downward, so that the stud is pressed into the keyboard workpiece 100.
As shown in fig. 8, the keyboard riveting machine of the present embodiment further includes a visual detection device 9. The visual inspection device 9 includes a third mounting bracket 91, a first inspection mechanism 92, and a second inspection mechanism 93. The third mounting frame 91 is mounted on the machine body 1 and erected on the periphery of the rotating disc 21, the first detection mechanism 92 is mounted on the inner side of the first suction conveying device 3 and located above the positioning jig 22, and the second detection mechanism 93 is mounted on the inner side of the third suction conveying device 5 and located above the positioning jig 22. The first detection mechanism 92 and the second detection mechanism 93 of the present embodiment are CCD vision detection modules, and may specifically include components such as a CCD camera and a light source.
Therefore, the first detection mechanism 92 can identify the stud input by the first suction conveying device 3 and feed back the corresponding position information to the control device, and the second detection mechanism 93 can identify the nut input by the third suction conveying device 5 and feed back the corresponding position information to the control device, so that accurate feeding and discharging are facilitated, and the production efficiency is improved.
As shown in fig. 6, the turntable device 2 further includes a driving module 23 for driving the rotary disc 21 to rotate, the driving module 23 is disposed below the rotary disc 21 and is in power connection with the rotary disc 21, and the positioning fixture 22 is provided with a first limiting groove (not shown) engaged with the stud and a second limiting groove (not shown) engaged with the keyboard workpiece 100. The drive module 23 of the present embodiment may be a rotary drive combination structure such as a rotary motor and a speed reducer for driving the rotary disk 21 to rotate.
As shown in fig. 7, the turntable device 2 further includes a positioning mechanism 24, the positioning fixture 22 is a movable positioning fixture 22 that can be lifted relative to the rotating disc 21, the positioning mechanism 24 is installed on the machine body 1 and located at the bottom of the rotating disc 21, and the positioning mechanism 24 is matched with the positioning fixture 22 for limiting the positioning fixture 22.
The positioning jig 22 includes an upper module 221, a lower module 222, and guide posts 223. The upper module 221 is arranged above the rotating disc 21, the lower module 222 is arranged below the rotating disc 21, the upper module 221 and the lower module 222 are connected through a guide column 223, and the guide column 223 penetrates through the rotating disc 21;
the positioning mechanism 24 includes a second driving member 241 and a positioning block 242. The second driving element 241 is installed on the machine body 1, and the positioning block 242 is installed at the driving end of the second driving element 241 and is in spacing fit with the lower module 222. The positioning block 242 of the present embodiment is further provided with a hemispherical positioning protrusion 242a on the upper end surface thereof, and the second driving member 241 is a telescopic cylinder.
Therefore, the positioning mechanism 24 can position and support the positioning fixture 22 to assist other devices to complete corresponding operations.
As shown in fig. 10 and 11, the riveting device 6 includes a fourth mounting bracket 61 and a riveting mechanism 62 mounted to the fourth mounting bracket 61. The riveting mechanism 62 includes a third driving member 621 and a riveting upper die 622. The riveting upper die 622 is mounted on the fourth mounting frame 61 and located above the upper die block 221 of the positioning fixture 22, and the third driving element 621 is mounted on the machine body 1 and located below the lower die block 222 of the positioning fixture 22. The fourth mounting frame 61 includes an upper frame body 611, a lower frame body 612, and a connection block 613 connecting the upper frame body 611 and the lower frame body 612. An accommodating cavity 620 for accommodating the riveting upper die 622, the positioning jig 22 and the rotating disc 21 is formed between the upper frame body 611 and the lower frame body 612. The riveting upper die 622 is fixedly mounted on the upper frame body 611 and located above the positioning jig 22, and the upper end of the third driving element 621 is fixed to the bottom of the lower frame body 612 and the driving end can lift up the positioning jig 22. The third driving member 621 of the present embodiment may be an electric cylinder. Therefore, when the positioning jig 22 rotates to the riveting station, the riveting mechanism works, the third driving part 621 jacks up the positioning jig 22, so that the whole positioning jig 22 rises, the upper module 221 is close to the riveting upper die 622 to complete die assembly, and riveting of the nut and the keyboard workpiece 100 is completed.
As shown in fig. 12, the blanking device 7 includes a single-shaft drive mechanism 71, a rotation mechanism 72, and a second suction mechanism 73. The single-shaft driving mechanism 71 is mounted on the machine body 1, the rotating mechanism 72 is mounted on the single-shaft driving mechanism 71, and the second material sucking mechanism 73 is mounted on the rotating mechanism 72 and is matched with the keyboard workpiece 100 in the positioning jig 22.
The single-shaft driving mechanism 71 of the present embodiment may be a linear driving module composed of a screw nut, a motor, a linear guide, a slider, and the like, which is a linear driving structure commonly used in the market, and the specific structure is not described. The rotating mechanism 72 may be a rotating motor, and the second sucking mechanism 73 may be a suction cup.
As shown in fig. 1 and 2, the keyboard riveting machine further comprises a feeding device 10 and a discharging device 20. The feeding device 10 and the discharging device 20 are arranged on the side of the machine body 1, the tail end of the feeding device 10 is positioned in front of the second material sucking and conveying device 4, and the front end of the discharging device 20 is positioned at the discharging tail end of the discharging device 7. The feeding device 10 and the discharging device 20 of the present embodiment may be belt lines.
The keyboard riveting machine provided by the invention realizes automation of feeding, discharging, detecting and riveting, is convenient for realizing automatic production of the keyboard, can improve the utilization rate, can reduce the labor input and saves the cost.
The keyboard riveting machine further comprises a control device. The rotary table device 2, the first material sucking and conveying device 3, the second material sucking and conveying device 4, the third material sucking and conveying device 5, the pressing device 8, the riveting device 6 and the blanking device 7 are all electrically connected with the control device. The control device of the present embodiment may be an industrial computer, a PLC controller, or the like.
The invention provides a keyboard riveting machine with a brand new structure, which has the following working operation principle:
a. the first material sucking and conveying device 3 sucks the stud and puts the stud on the positioning jig 22 of the rotating disc 21;
b. the rotating disc 21 rotates to drive the positioning jig 22 containing the studs to move to the rear of the second material suction and conveying device 4, and the second material suction and conveying device 4 sucks the keyboard workpiece 100 on the belt of the feeding device 10 and places the keyboard workpiece 100 on the positioning jig 22, so that the keyboard workpiece 100 falls on the studs;
c. the rotating disc 21 continues to rotate, the positioning jig 22 containing the studs and the keyboard workpiece 100 is driven to move to the rear of the third material suction and conveying device 5, the pressing device 8 works to press the keyboard workpiece 100 downwards, so that the studs are riveted on the keyboard workpiece 100, and then the third material suction and conveying device 5 sucks the nuts and puts the nuts on the keyboard workpiece 100;
d. the rotating disc 21 continues to rotate, so that the positioning jig 22 rotates to the riveting station, and the riveting device 6 rivets the nut on the keyboard workpiece 100;
e. the rotating disc 21 continues to rotate to the blanking station, and the blanking device 7 takes the materials from the positioning jig 22 and outputs the materials to the belt of the discharging device 20.
Therefore, the keyboard riveting machine provided by the invention realizes automation of loading, unloading, detection and riveting, facilitates automatic production of the keyboard, can improve the utilization rate, can reduce the manpower input and saves the cost. The specific riveting CT can be lifted from 10s/pcs to 3.5 s/pcs; manpower is reduced from 10 to 1 person.
What has been described above are merely some embodiments of the present invention. It will be apparent to those skilled in the art that various changes and modifications can be made without departing from the inventive concept thereof, and these changes and modifications can be made without departing from the spirit and scope of the invention.