CN113798886A - Pneumatic clamp for machining centre hole of convex fork - Google Patents
Pneumatic clamp for machining centre hole of convex fork Download PDFInfo
- Publication number
- CN113798886A CN113798886A CN202010539142.0A CN202010539142A CN113798886A CN 113798886 A CN113798886 A CN 113798886A CN 202010539142 A CN202010539142 A CN 202010539142A CN 113798886 A CN113798886 A CN 113798886A
- Authority
- CN
- China
- Prior art keywords
- center
- base
- fork
- convex
- rod
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000003754 machining Methods 0.000 title claims description 11
- 238000005553 drilling Methods 0.000 claims description 13
- 230000001360 synchronised effect Effects 0.000 description 4
- 239000011111 cardboard Substances 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 2
- 238000010276 construction Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 230000007306 turnover Effects 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q3/00—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine
- B23Q3/02—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine for mounting on a work-table, tool-slide, or analogous part
- B23Q3/06—Work-clamping means
- B23Q3/08—Work-clamping means other than mechanically-actuated
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q3/00—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine
- B23Q3/02—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine for mounting on a work-table, tool-slide, or analogous part
- B23Q3/06—Work-clamping means
- B23Q3/062—Work-clamping means adapted for holding workpieces having a special form or being made from a special material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q2703/00—Work clamping
- B23Q2703/02—Work clamping means
- B23Q2703/04—Work clamping means using fluid means or a vacuum
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Jigs For Machine Tools (AREA)
Abstract
The invention relates to a pneumatic clamp for processing a centre hole of a convex circular fork, belonging to the field of processing facilities, which adopts a rectangular base, a rectangular vertical plate is respectively vertically arranged on two sides of the upper surface of the base in the longitudinal direction, a cylindrical positioning rod is respectively horizontally arranged on two sides of the upper part between the two vertical plates in the transverse direction, two L-shaped clamping plates are oppositely arranged on the upper surfaces of the two positioning rods, a cylindrical central shaft is vertically arranged in the center of the upper surface of the base, a disc-shaped rotating disc is arranged on the upper surface of the central shaft, the front side and the rear side of the rotating disc are respectively connected with the bottom of each corresponding clamping plate through a long-strip-shaped connecting rod, the front side of the rotating disc is connected with the air cylinder through a rectangular pull rod, when the convex fork is vertically placed on the rotary table, the air cylinder pushes the rotary table to rotate, and the rotary table synchronously pulls the two clamping plates to the center through the two connecting rods so as to force the two clamping plates to clamp the convex fork.
Description
Technical Field
The invention discloses a pneumatic clamp for machining a centre hole of a convex circular fork, belongs to the field of machining facilities, and particularly relates to synchronous clamping of two L-shaped clamps through a pneumatic turntable.
Background
A convex fork thimble hole and a thimble fixing hole on the lathe tailstock when a lathe is used for processing the convex fork. Because the protruding circle fork is the C type, can't use the chuck of grabbing from centering three of lathe self when the thimble hole of processing protruding circle fork rear end, consequently need just can process it after fixing the protruding circle fork with the help of anchor clamps. The enterprise of the existing convex fork production is processing the convex fork, the center holes at the front end and the rear end of the convex fork are processed firstly, then the convex fork is fixed on a numerical control lathe by means of a clamp for accurate processing, when the rear center hole of the convex fork is processed, the front surface of the convex fork is a C-shaped self-centering three-grab chuck which cannot use the lathe, the convex fork is basically fixed by adopting a four-grab non-self-centering chuck, and the four-grab non-self-centering chuck cannot realize synchronous opening and closing of the four grabs and needs workers to adjust the convex fork. Therefore, a clamp capable of quickly self-centering a special-shaped piece is needed to replace the existing non-self-centering four-grab chuck.
Disclosure of Invention
The pneumatic clamp for processing the thimble hole of the convex circular fork overcomes the difficulties, adopts the rectangular base, a rectangular vertical plate is respectively vertically arranged on two sides of the upper surface of the base in the longitudinal direction, a cylindrical positioning rod is respectively horizontally arranged on two sides of the upper part between the two vertical plates in the transverse direction, two L-shaped clamping plates are oppositely arranged on the upper surfaces of the two positioning rods, a cylindrical central shaft is vertically arranged in the center of the upper surface of the base, a disc-shaped rotating disc is arranged on the upper surface of the central shaft, the front side and the rear side of the rotating disc are respectively connected with the bottom of each corresponding clamping plate through a long-strip-shaped connecting rod, the front side of the rotating disc is connected with the air cylinder through a rectangular pull rod, when the convex fork is vertically placed on the rotary table, the air cylinder pushes the rotary table to rotate, and the rotary table synchronously pulls the two clamping plates to the center through the two connecting rods so as to force the two clamping plates to clamp the convex fork.
A pneumatic clamp for machining a centre hole of a convex circular fork is characterized by comprising a base, a vertical plate, a positioning rod, a clamping plate, a central shaft, a rotary plate, a pull rod, a cylinder, a connecting rod, a clamping groove, a sliding hole, an electric control reversing valve and an air pipe;
the base is rectangular, the centers of the two ends of the base are horizontally arranged on a platform of the bench drilling machine through bolts, the two ends of the base are vertically provided with a rectangular vertical plate, the two sides above the two vertical plates are respectively and vertically provided with a cylindrical positioning rod, and the two positioning rods are horizontally and parallelly arranged.
The clamping plates are L-shaped, one clamping plate is arranged on each of two sides of the two positioning rods, the two clamping plates are arranged in opposite directions, a V-shaped clamping groove is formed in the center of the thinner end of each clamping plate, a circular sliding hole is horizontally formed below each of two sides of the thicker end of each clamping plate, and the sliding holes in two sides below the two clamping plates are respectively arranged on the two positioning rods;
the central shaft is cylindrical and is vertically arranged in the center of the upper surface of the base, the top end of the upper surface of the central shaft is horizontally provided with a disc-shaped turntable, and the front and rear symmetrical parts of the bottom of the turntable are respectively provided with a ball head;
the left side of the front connecting rod is connected with the center of the bottom of the left clamping plate of the positioning rod through a ball head, the right side of the front connecting rod is connected with the ball head below the front of the turntable, the left side of the rear connecting rod is connected with the ball head below the rear of the turntable, and the right side of the rear connecting rod is connected with the center of the bottom of the right clamping plate of the positioning rod through the ball head;
the cylinder is cylindrical and is transversely and horizontally arranged above the left side of the front of the base, the top end of the left side of the cylinder is connected with the center of the front of the left vertical plate on the base, and the right top end of the right piston rod of the cylinder is connected with the front of the long-strip-shaped pull rod horizontally arranged in front of the rotary table through a pin shaft;
the electric control reversing valve is arranged at the back of the drilling machine, a front channel and a rear channel of the electric control reversing valve are respectively connected with two cavities of the air cylinder through air pipes, an air inlet of the electric control reversing valve is connected with a pump station through the air pipes, and the electric control reversing valve is connected with a control box of the drilling machine through a power line.
The center point of the center shaft and the center point of the center drill below the calipers of the drilling machine after the two clamping grooves are folded are on the same straight line.
Has the advantages that: the enterprise of the existing convex fork production is processing the convex fork, the center holes at the front end and the rear end of the convex fork are processed firstly, then the convex fork is fixed on a numerical control lathe by means of a clamp for accurate processing, when the rear center hole of the convex fork is processed, the front surface of the convex fork is a C-shaped self-centering three-grab chuck which cannot use the lathe, the convex fork is basically fixed by adopting a four-grab non-self-centering chuck, and the four-grab non-self-centering chuck cannot realize synchronous opening and closing of the four grabs and needs workers to adjust the convex fork. The utility model provides a pneumatic fixture of processing protruding circle fork thimble hole, adopt rectangular base, a rectangular riser is vertically installed respectively to both sides on the base, a columniform locating lever is respectively transversely installed to both sides horizontal level in top between two risers, the splint of two L types are installed to the higher authority subtend of two locating levers, the central authorities on the base install columniform center pin perpendicularly, the carousel of disc is installed to the higher authority of center pin, both sides respectively are connected with the bottom that corresponds the cardboard separately through a long banding connecting rod respectively around the carousel, the place ahead of carousel is connected with the cylinder through rectangular pull rod, place perpendicularly behind the higher authority of carousel when protruding circle fork, the cylinder promotes the carousel rotatory, the carousel pulls two cardboards to the center through two connecting rods are synchronous, force two cardboards to press from both sides protruding circle fork tightly.
Drawings
FIG. 1 is a front view of a pneumatic fixture for machining a hole in the top of a cam fork;
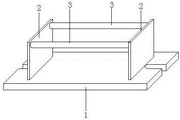
FIG. 2 is a schematic structural view of a base, a vertical plate and a positioning rod;
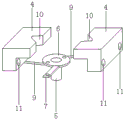
FIG. 3 is a schematic structural view of a clamping plate, a central shaft, a rotary table, a pull rod, a connecting rod, a clamping groove and a sliding hole;
FIG. 4 is a schematic view of the connection of the electrically controlled directional control valve with the cylinder through the air pipe;
the marks in the above figures are a base 1, a vertical plate 2, a positioning rod 3, a clamping plate 4, a central shaft 5, a rotary table 6, a pull rod 7, a cylinder 8, a connecting rod 9, a clamping groove 10, a sliding hole 11, an electric control reversing valve 12 and an air pipe 13.
Detailed Description
The shape and construction of the present invention will now be described in detail with reference to the accompanying drawings and reference numerals:
a pneumatic clamp for machining a centre hole of a convex circular fork is characterized by comprising a base 1, a vertical plate 2, a positioning rod 3, a clamping plate 4, a central shaft 5, a rotary table 6, a pull rod 7, an air cylinder (8kpa)8, a connecting rod 9, a clamping groove 10, a sliding hole 11, an electric control reversing valve (8kpa, DC12V)12 and an air pipe (8kpa) 13;
the base 1 is rectangular, the centers of the two ends of the base are horizontally arranged on a platform of the bench drilling machine through bolts, a rectangular vertical plate 2 is vertically arranged at each of the two ends of the base 1, and two sides above the two vertical plates 2 are horizontally and parallelly arranged between a cylindrical positioning rod 3 and two positioning rods 3.
The clamping plates 4 are L-shaped, one clamping plate is arranged on each of two sides of the two positioning rods 3, the two clamping plates 4 are arranged in opposite directions, a V-shaped clamping groove 10 is arranged in the center of the thinner end of each clamping plate 4, a circular sliding hole 11 is horizontally arranged below each of two sides of the thicker end of each clamping plate 4, and the sliding holes 11 on two sides below the two clamping plates 4 are respectively arranged on the two positioning rods 3;
the central shaft 5 is cylindrical and is vertically arranged in the center of the upper surface of the base 1, a disc-shaped turntable 6 is horizontally arranged at the top end of the upper surface of the central shaft 5, and a ball head is respectively arranged at the symmetrical positions of the front side and the rear side of the bottom of the turntable 6;
the connecting rod 9 is long-strip-shaped, the front and the rear of the turntable 6 are respectively provided with one connecting rod, the left side of the front connecting rod 9 is connected with the center of the bottom of the left clamping plate 4 of the positioning rod 3 through a ball head, the right side of the front connecting rod 9 is connected with the ball head below the front of the turntable 6, the left side of the rear connecting rod 9 is connected with the ball head below the rear of the turntable 6, and the right side of the rear connecting rod 9 is connected with the center of the bottom of the right clamping plate 4 of the positioning rod 3 through the ball head;
the cylinder 8 is cylindrical and is transversely and horizontally arranged above the left side of the front surface of the base 1, the top end of the left side of the cylinder 8 is connected with the center of the front part of the left vertical plate 2 on the base 1, and the right top end of the right piston rod of the cylinder 8 is connected with the front part of a long-strip-shaped pull rod 7 horizontally arranged in front of the rotary table 6 through a pin shaft;
the electronic control reversing valve 12 is arranged behind the drilling machine, a front channel and a rear channel of the electronic control reversing valve 12 are respectively connected with two cavities of the air cylinder 8 through air pipes 13, an air inlet of the electronic control reversing valve 12 is connected with a pump station through the air pipes 13, and the electronic control reversing valve 12 is connected with a control box of the drilling machine through a power line.
The central point of the central shaft 5 and the two clamping grooves 10 after being folded is on the same straight line with the central point of the central drill below the calipers of the drilling machine.
When the pneumatic clamp for machining the center hole of the convex fork is used, a worker firstly turns on a pump station and a power supply, places the front part (C-shaped fork) of the unprocessed convex fork on the rotary table to enable the convex fork to be vertical, holds the top end of the convex fork by one hand, presses down a switch on the control box by one hand, controls an electric control reversing valve by a controller in the control box to drive a left cavity of a cylinder to push a piston rod to the right through high-pressure gas, the piston rod pushes the rotary table to rotate anticlockwise through a pull rod, the rotary table simultaneously pulls two connecting rods to move oppositely and drives the two clamping plates to move synchronously towards the central part of the central shaft so that the two clamping plates synchronously clamp the upper part of the convex fork, at the moment, the worker quickly operates the central shaft of a drilling machine to descend, forces a central drill a conical center hole in the top part of the convex fork through a central drill and then quickly resets the central shaft, a worker presses a switch on the control box again, a controller in the control box controls the electric control reversing valve to drive a right cavity of the air cylinder to force the piston rod to be pushed out leftwards through high-pressure air, the piston rod pulls the rotary table to rotate clockwise through the pull rod, the rotary table simultaneously pushes the two connecting rods to move in opposite directions and drives the two clamping plates to move towards the two sides of the central shaft synchronously, the two clamping plates synchronously loosen the convex circular forks, the worker quickly unloads the convex circular forks with the top pin holes on the turnover vehicle, and then the top pin holes are drilled on the unprocessed convex circular forks repeatedly according to the steps.
The above-mentioned non-detailed description is prior art.
The foregoing is merely a general disclosure of the invention and is not intended to limit the invention in any way; those skilled in the art should appreciate that they can readily use the disclosed conception and specific embodiments as a basis for designing or modifying other structures for carrying out the same purposes of the present invention without departing from the scope of the invention as defined by the appended claims.
Claims (3)
1. A pneumatic clamp for machining a centre hole of a convex circular fork is characterized by comprising a base, a vertical plate, a positioning rod, a clamping plate, a central shaft, a rotary plate, a pull rod, a cylinder, a connecting rod, a clamping groove, a sliding hole, an electric control reversing valve and an air pipe;
the base is rectangular, the centers of the two ends of the base are horizontally arranged on a platform of the bench drilling machine through bolts, the two ends of the base are vertically provided with a rectangular vertical plate, the two sides above the two vertical plates are respectively and vertically provided with a cylindrical positioning rod, and the two positioning rods are horizontally and parallelly arranged.
2. The pneumatic clamp for machining the thimble hole of the convex fork as claimed in claim 1, wherein the clamping plate is L-shaped, one clamping plate is respectively arranged at two sides of the two positioning rods, the two clamping plates are arranged oppositely, a V-shaped clamping groove is respectively arranged at the center of the thinner end of the upper surface of each clamping plate, a circular sliding hole is respectively and horizontally arranged below two sides of the thicker end of each clamping plate, and the sliding holes at two sides below the two clamping plates are respectively arranged on the upper surfaces of the two positioning rods;
the central shaft is cylindrical and is vertically arranged in the center of the upper surface of the base, the top end of the upper surface of the central shaft is horizontally provided with a disc-shaped turntable, and the front and rear symmetrical parts of the bottom of the turntable are respectively provided with a ball head;
the left side of the front connecting rod is connected with the center of the bottom of the left clamping plate of the positioning rod through a ball head, the right side of the front connecting rod is connected with the ball head below the front of the turntable, the left side of the rear connecting rod is connected with the ball head below the rear of the turntable, and the right side of the rear connecting rod is connected with the center of the bottom of the right clamping plate of the positioning rod through the ball head;
the cylinder is cylindrical and is transversely and horizontally arranged above the left side of the front of the base, the top end of the left side of the cylinder is connected with the center of the front of the left vertical plate on the base, and the right top end of the right piston rod of the cylinder is connected with the front of the long-strip-shaped pull rod horizontally arranged in front of the rotary table through a pin shaft;
the electric control reversing valve is arranged at the back of the drilling machine, a front channel and a rear channel of the electric control reversing valve are respectively connected with two cavities of the air cylinder through air pipes, an air inlet of the electric control reversing valve is connected with a pump station through the air pipes, and the electric control reversing valve is connected with a control box of the drilling machine through a power line.
3. The pneumatic clamp for machining the center hole of the convex fork as claimed in claim 1 or 2, wherein the center point of the center shaft and the two clamping grooves after being closed is collinear with the center point of the center drill below the calipers of the drilling machine.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010539142.0A CN113798886A (en) | 2020-06-14 | 2020-06-14 | Pneumatic clamp for machining centre hole of convex fork |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010539142.0A CN113798886A (en) | 2020-06-14 | 2020-06-14 | Pneumatic clamp for machining centre hole of convex fork |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN113798886A true CN113798886A (en) | 2021-12-17 |
Family
ID=78944212
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010539142.0A Pending CN113798886A (en) | 2020-06-14 | 2020-06-14 | Pneumatic clamp for machining centre hole of convex fork |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN113798886A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116480798A (en) * | 2023-03-24 | 2023-07-25 | 江苏汇浦新材科技股份有限公司 | A New Ceramic Composite Metal Ball Valve |
-
2020
- 2020-06-14 CN CN202010539142.0A patent/CN113798886A/en active Pending
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116480798A (en) * | 2023-03-24 | 2023-07-25 | 江苏汇浦新材科技股份有限公司 | A New Ceramic Composite Metal Ball Valve |
| CN116480798B (en) * | 2023-03-24 | 2025-09-30 | 江苏汇浦新材科技股份有限公司 | A new type of ceramic composite metal ball valve |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204771752U (en) | Spindle adds clamping apparatus | |
| WO2018166181A1 (en) | Flexible clamp and method for use in milling blades having large complex curved surfaces | |
| CN102328231B (en) | Flexible clamp for numerical-control processing and application thereof | |
| CN214868947U (en) | Rotation type frock clamp suitable for numerical control of multiple model gate valve processing | |
| CN110216481A (en) | Numerical control vertical machine tool and method for processing valve body using it | |
| CN201172190Y (en) | Multifunction quick change double-moving jaw bench vice | |
| CN212311481U (en) | Pneumatic clamp for machining centre hole of convex fork | |
| CN204771646U (en) | Mechanism in automatic correction of branch of spindle | |
| CN104942615A (en) | Industrial robot transmission shaft key groove machining fixture | |
| CN116944894A (en) | Full-automatic assembly line of production shoes mould | |
| CN206567825U (en) | A kind of Novel drill tapping dual-purpose tool workpiece rotary table structure | |
| CN205271439U (en) | Tight positioner of clamp of pneumatic type ring flange | |
| CN210451375U (en) | Clamping mechanism and base body positioning device of laser welding machine for diamond thin-wall drill | |
| CN204771648U (en) | Industrial robot transmission shaft keyway add clamping apparatus | |
| CN110948264B (en) | A connecting beam drilling fixture | |
| CN116690160A (en) | Valve seat positioning press-fitting mechanism and control method thereof | |
| CN203437853U (en) | Manual-automatic integrated welding clamp | |
| CN210878670U (en) | Universal fixture for milling the inner and outer sides and both ends of cylindrical workpieces | |
| CN203863394U (en) | Clamp special for combined drilling of transmission control connection assembly | |
| CN203611015U (en) | Cross slip ring clamping tool | |
| CN214603115U (en) | Aviation aluminum alloy workpiece clamp for milling | |
| CN223506227U (en) | Lathe machining device applied to rough machining of piston | |
| CN220480840U (en) | Novel valve core valve rod automatic assembly machine | |
| CN206382600U (en) | A kind of accurate hole positioner of processing three-jaw flange side surface three | |
| CN221134693U (en) | Positioning device for positioning groove type workpiece |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20211217 |
|
| WD01 | Invention patent application deemed withdrawn after publication |