CN113584536A - Screw surface rapid electroplating process and device thereof - Google Patents
Screw surface rapid electroplating process and device thereof Download PDFInfo
- Publication number
- CN113584536A CN113584536A CN202110897952.8A CN202110897952A CN113584536A CN 113584536 A CN113584536 A CN 113584536A CN 202110897952 A CN202110897952 A CN 202110897952A CN 113584536 A CN113584536 A CN 113584536A
- Authority
- CN
- China
- Prior art keywords
- screw
- electroplating
- power supply
- screw rod
- surface rapid
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000009713 electroplating Methods 0.000 title claims abstract description 57
- 238000000034 method Methods 0.000 title claims abstract description 25
- 238000009434 installation Methods 0.000 claims abstract description 28
- 238000004140 cleaning Methods 0.000 claims abstract description 13
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 10
- 238000001035 drying Methods 0.000 claims abstract description 7
- 239000000126 substance Substances 0.000 claims abstract description 7
- 239000011810 insulating material Substances 0.000 claims abstract description 4
- 238000005406 washing Methods 0.000 claims abstract description 4
- 238000007747 plating Methods 0.000 claims description 17
- 238000005246 galvanizing Methods 0.000 claims description 13
- 238000004506 ultrasonic cleaning Methods 0.000 claims description 7
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 claims description 6
- 239000003513 alkali Substances 0.000 claims description 6
- 239000011701 zinc Substances 0.000 claims description 6
- 229910052725 zinc Inorganic materials 0.000 claims description 6
- 239000012535 impurity Substances 0.000 claims description 5
- PTFCDOFLOPIGGS-UHFFFAOYSA-N Zinc dication Chemical compound [Zn+2] PTFCDOFLOPIGGS-UHFFFAOYSA-N 0.000 claims description 3
- 238000005238 degreasing Methods 0.000 claims description 3
- 238000004945 emulsification Methods 0.000 claims description 3
- 238000006479 redox reaction Methods 0.000 claims description 3
- 238000007127 saponification reaction Methods 0.000 claims description 3
- NWONKYPBYAMBJT-UHFFFAOYSA-L zinc sulfate Chemical compound [Zn+2].[O-]S([O-])(=O)=O NWONKYPBYAMBJT-UHFFFAOYSA-L 0.000 claims description 3
- 239000000243 solution Substances 0.000 description 19
- 229910052751 metal Inorganic materials 0.000 description 5
- 239000002184 metal Substances 0.000 description 5
- 239000012670 alkaline solution Substances 0.000 description 2
- 230000005540 biological transmission Effects 0.000 description 2
- 238000006243 chemical reaction Methods 0.000 description 2
- 238000004891 communication Methods 0.000 description 2
- 238000005260 corrosion Methods 0.000 description 2
- 230000007797 corrosion Effects 0.000 description 2
- 238000005868 electrolysis reaction Methods 0.000 description 2
- 150000002739 metals Chemical class 0.000 description 2
- 238000003825 pressing Methods 0.000 description 2
- 229910045601 alloy Inorganic materials 0.000 description 1
- 239000000956 alloy Substances 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 229910000365 copper sulfate Inorganic materials 0.000 description 1
- ARUVKPQLZAKDPS-UHFFFAOYSA-L copper(II) sulfate Chemical compound [Cu+2].[O-][S+2]([O-])([O-])[O-] ARUVKPQLZAKDPS-UHFFFAOYSA-L 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 230000002708 enhancing effect Effects 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 230000003647 oxidation Effects 0.000 description 1
- 238000007254 oxidation reaction Methods 0.000 description 1
Images



Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D3/00—Electroplating: Baths therefor
- C25D3/02—Electroplating: Baths therefor from solutions
- C25D3/22—Electroplating: Baths therefor from solutions of zinc
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23G—CLEANING OR DE-GREASING OF METALLIC MATERIAL BY CHEMICAL METHODS OTHER THAN ELECTROLYSIS
- C23G1/00—Cleaning or pickling metallic material with solutions or molten salts
- C23G1/14—Cleaning or pickling metallic material with solutions or molten salts with alkaline solutions
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D17/00—Constructional parts, or assemblies thereof, of cells for electrolytic coating
- C25D17/06—Suspending or supporting devices for articles to be coated
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D5/00—Electroplating characterised by the process; Pretreatment or after-treatment of workpieces
- C25D5/34—Pretreatment of metallic surfaces to be electroplated
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Electrochemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Electroplating Methods And Accessories (AREA)
Abstract
The invention discloses a screw surface rapid electroplating process in the field of electroplating, which comprises the following steps: step one, chemical oil removal; step two, hot water washing, step three, electroplating; and step four, cleaning and drying. The invention also discloses a device for the screw rod surface rapid electroplating process, which comprises an electroplating box, wherein a power supply is arranged on the outer wall of the right side of the electroplating box, a loading mechanism extending into the electroplating box is arranged on the left side of the electroplating box, a hydraulic cylinder is arranged on the loading mechanism, a telescopic rod of the hydraulic cylinder is connected with an installation sleeve, the installation sleeve is made of an insulating material, an electrode plate is arranged in the installation sleeve and is electrically connected with the power supply through a second lead, two clamping devices are arranged in the installation sleeve on the upper side of the electrode plate, a screw rod extending out of the installation sleeve is arranged between the two clamping devices, and the bottom of the screw rod is attached to the electrode plate. The invention has convenient installation and disassembly of the screw and high electroplating efficiency.
Description
Technical Field
The invention relates to the field of electroplating, in particular to a screw surface rapid electroplating process and a device thereof.
Background
Electroplating is a process of plating a thin layer of other metals or alloys on the surface of some metals by using the principle of electrolysis, and is a process of attaching a layer of metal film on the surface of a metal or other material product by using the action of electrolysis, thereby having the effects of preventing metal oxidation (such as corrosion), improving wear resistance, conductivity, light reflection, corrosion resistance (such as copper sulfate and the like), enhancing the appearance and the like. The outer layer of many coins is also plated.
At present, the screw rod is rustproof by adopting a galvanizing method, the screw rod is required to be connected with a power supply when the screw rod is galvanized, the conventional galvanizing device is troublesome when the screw rod is connected with the power supply, more time can be wasted, and the electroplating efficiency is reduced.
Disclosure of Invention
The invention aims to provide a screw surface rapid electroplating process and a device thereof, which are used for solving the problems in the background technology.
In order to achieve the purpose, the invention provides the following technical scheme:
a screw surface rapid electroplating process comprises the following steps: step one, chemical degreasing: adding the screw into hot alkali solution, and removing oil stains on the surface of the screw through saponification and emulsification of the hot alkali solution on oil; step two, hot water washing: adding hot water into an ultrasonic cleaning machine, and then adding the screw rod after oil removal into the ultrasonic cleaning machine for cleaning to remove impurities on the surface of the screw rod; step three, electroplating: putting the cleaned screw into a galvanizing solution, connecting the screw with a power supply, and converting zinc ions in the electroplating solution into simple substance zinc to cover the surface of the screw through oxidation-reduction reaction; step four, cleaning and drying: and (4) placing the galvanized screw into clear water to be cleaned once, taking out the screw after cleaning, and drying and storing.
As a further scheme of the invention: the zinc plating solution is alkaline zincate plating solution.
As a further scheme of the invention: the temperature of the galvanizing solution is 0-50 ℃.
The utility model provides a device of quick electroplating process in screw rod surface, includes the electroplating box, install the power on the right side outer wall of electroplating box, install the anode rod on the right side inner wall of electroplating box, the anode rod is through first wire and power electric connection, the left side of electroplating box is installed and is extended to its inside mechanism of going up, it installs the pneumatic cylinder in the mechanism to go up, the telescopic link and the installing sleeve of pneumatic cylinder link to each other, the installing sleeve adopts insulating material to make, the internally mounted of installing sleeve has the electrode slice, the electrode slice passes through second wire and power electric connection, a plurality ofly and the first spring of the inside bottom elastic connection of installing sleeve are installed to the bottom of electrode slice, two clamping device are installed in the installing sleeve to the upside of electrode slice, clamping device includes: splint and second spring, splint pass through the inner wall elastic connection of a plurality of second springs and installation cover, two install between the clamping device and extend to the outside screw rod of installation cover, the bottom and the electrode piece of screw rod laminate mutually.
As a further scheme of the invention: the power supply is a direct current power supply.
As a further scheme of the invention: the mechanism of going up includes: step motor, action wheel, follow driving wheel, drive belt, pivot and eccentric rotary table, step motor is fixed in the left side of electroplating box, install the action wheel on step motor's the output shaft, install from the driving wheel in the top of action wheel, it is connected with the action wheel rotation through the drive belt to follow the driving wheel, install in the pivot from the driving wheel, the pivot extends to and electroplates the incasement and links to each other with eccentric rotary table, the pivot passes through the bearing and is connected with electroplating box rotation, install the pneumatic cylinder on the eccentric rotary table.
As a further scheme of the invention: the stepper motor rotates 180 degrees each time.
As a further scheme of the invention: the diameter ratio of the driving wheel to the driven wheel is 1: 1.
compared with the prior art, the invention has the beneficial effects that: the screw surface rapid electroplating process and the device thereof, during electroplating, firstly removing oil stains on the surface of a screw through hot alkaline solution, then removing impurities on the screw through an ultrasonic cleaner, then pressing the screw into an installation sleeve, at the moment, the opening of the installation sleeve faces upwards, leading the bottom of the screw to be attached to an electrode sheet, leading the communication between the screw and a power supply to be more convenient, leading a clamping plate to be driven by the elasticity of a second spring to clamp the screw, then starting a stepping motor to drive a driving wheel to rotate through the stepping motor, leading a driven wheel to rotate through the rotation of the driving wheel, leading a rotating shaft and an eccentric turntable to rotate through the driven wheel, leading a hydraulic cylinder and the installation sleeve to rotate through the eccentric turntable, leading the opening of the installation sleeve to face downwards, leading the installation sleeve to move downwards, leading the screw to be immersed in a galvanizing solution through the driving of the installation sleeve, then turning on the power supply to carry out galvanizing reaction, after the galvanization is finished, the hydraulic cylinder and the installation sleeve are driven to overturn through the workpiece feeding mechanism, so that the opening of the installation sleeve faces upwards, the screw rod is extracted, and finally, the workpiece is cleaned and dried. In conclusion, the screw rod is convenient to mount and dismount, and the electroplating efficiency is high.
Drawings
FIG. 1 is a flow chart of the screw surface rapid plating process of the present invention.
FIG. 2 is a view showing an apparatus for a rapid plating process on the surface of a screw according to the present invention.
Fig. 3 is an internal cross-sectional view of fig. 2 of the present invention.
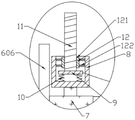
Fig. 4 is a partial view at a of fig. 3 of the present invention.
Fig. 5 is a schematic diagram of the loading mechanism of fig. 3 in an inverted state.
In the figure: 1-electroplating box, 2-power supply, 3-anode bar, 4-first lead, 5-second lead, 6-loading mechanism, 601-stepping motor, 602-driving wheel, 603-driven wheel, 604-driving belt, 605-rotating shaft, 606-eccentric turntable, 7-hydraulic cylinder, 8-mounting sleeve, 9-electrode plate, 10-first spring, 11-screw rod, 12-clamping device, 121-clamping plate and 122-second spring.
Detailed Description
In order to make the objects, technical solutions and advantages of the embodiments of the present invention clearer, the technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the drawings in the embodiments of the present invention, and it is obvious that the described embodiments are some, but not all, embodiments of the present invention. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
In the description of the embodiments of the present invention, it should be noted that the terms "first", "second" and "third" are used for the sake of clarity in describing the numbering of the components of the product and do not represent any substantial difference, unless explicitly stated or limited otherwise. The directions of "up", "down", "left" and "right" are all based on the directions shown in the attached drawings. Specific meanings of the above terms in the embodiments of the present invention can be understood by those of ordinary skill in the art according to specific situations.
It is to be understood that, unless otherwise expressly specified or limited, the term "coupled" is used broadly, and may, for example, refer to directly coupled devices or indirectly coupled devices through intervening media. Specific meanings of the above terms in the embodiments of the invention will be understood to those of ordinary skill in the art in specific cases.
Examples
Referring to fig. 1, in an embodiment of the present invention, a screw surface rapid plating process includes the following steps:
step one, chemical degreasing: adding the screw into hot alkali solution, and removing oil stains on the surface of the screw through saponification and emulsification of the hot alkali solution on oil; step two, hot water washing: hot water is added into the ultrasonic cleaning machine, the screw rod after being deoiled is added into the ultrasonic cleaning machine for cleaning, impurities on the surface of the screw rod are removed, the cleaning speed can be increased through the cleaning of the ultrasonic cleaning machine, and the cleaning is cleaner;
step three, electroplating: putting the cleaned screw into a galvanizing solution, connecting the screw with a power supply, and converting zinc ions in the electroplating solution into simple substance zinc to cover the surface of the screw through oxidation-reduction reaction, wherein the galvanizing solution is an alkaline zincate plating solution, and the temperature of the galvanizing solution is 0-50 ℃;
step four, cleaning and drying: and (4) placing the galvanized screw into clear water to be cleaned once, taking out the screw after cleaning, and drying and storing.
Referring to fig. 2-5, in an embodiment of the present invention, an apparatus for a screw surface rapid electroplating process includes an electroplating tank 1, a zinc plating solution is stored in the electroplating tank 1, a power supply 2 is installed on an outer wall of a right side of the electroplating tank 1, the power supply 2 is a direct current power supply, an anode rod 3 is installed on an inner wall of the right side of the electroplating tank 1, the anode rod 3 is electrically connected to the power supply 2 through a first wire 4, a workpiece loading mechanism 6 extending into the electroplating tank 1 is installed on a left side of the electroplating tank 1, a hydraulic cylinder 7 is installed on the workpiece loading mechanism 6, and the workpiece loading mechanism 6 includes: the electroplating device comprises a stepping motor 601, a driving wheel 602, a driven wheel 603, a transmission belt 604, a rotating shaft 605 and an eccentric turntable 606, wherein the stepping motor 601 is fixed on the left side of the electroplating box 1, the stepping motor 601 rotates 180 degrees every time, the driving wheel 602 is installed on an output shaft of the stepping motor 601, the driven wheel 603 is installed above the driving wheel 602, the driven wheel 603 is rotatably connected with the driving wheel 602 through the transmission belt 604, and the diameter ratio of the driving wheel 602 to the driven wheel 603 is 1: 1, follow driving wheel 603 and install on pivot 605, pivot 605 extends to and links to each other with eccentric rotating disc 606 in the electroplating box 1, pivot 605 passes through the bearing and is connected with electroplating box 1 rotation, install pneumatic cylinder 7 on the eccentric rotating disc 606, the telescopic link of pneumatic cylinder 7 links to each other with installation cover 8, installation cover 8 adopts insulating material to make, the internally mounted of installation cover 8 has electrode piece 9, electrode piece 9 passes through second wire 5 and power 2 electric connection, a plurality of and the inside bottom elastic connection's of installation cover first spring 10 is installed to the bottom of electrode piece 9, two clamping device 12 are installed to the upside of electrode piece 9 in installation cover 8, clamping device 12 includes: the clamping plate 121 is elastically connected with the inner wall of the mounting sleeve 8 through a plurality of second springs 122, a screw rod 11 extending to the outside of the mounting sleeve 8 is installed between the clamping devices 12, and the bottom of the screw rod 11 is attached to the electrode plate 9.
The screw rod surface rapid electroplating process and the device thereof, during electroplating, firstly removing oil stains on the surface of the screw rod by hot alkaline solution, then removing impurities on the screw rod by an ultrasonic cleaner, then pressing the screw rod into the mounting sleeve 8, at the moment, the opening of the mounting sleeve 8 faces upwards, leading the bottom of the screw rod to be attached to the electrode plate 9, leading the communication between the screw rod and the power supply 2 to be more convenient, driving the clamping plate 121 to clamp the screw rod by the elasticity of the second spring 122, then starting the stepping motor 601, driving the driving wheel 602 to rotate by the stepping motor 601, driving the driven wheel 603 to rotate by the rotation of the driving wheel 602, driving the rotating shaft 605 and the eccentric turntable 606 to rotate by the driven wheel 603, driving the hydraulic cylinder 7 and the mounting sleeve 8 to rotate by the eccentric turntable 606, leading the opening of the mounting sleeve 8 to face downwards, then driving the mounting sleeve 8 to move downwards by the hydraulic cylinder 7, and driving the screw rod 11 to move downwards by the mounting sleeve 8, make 11 submergions of screw rod in zinc-plating solution, open power 2 again and carry out the galvanizing reaction, after the galvanizing, drive pneumatic cylinder 7 and the upset of installation cover 8 through last mechanism 6 for the opening of installation cover 8 up, extract the screw rod, wash at last dry can, make the installation and the dismantlement of screw rod more convenient, improve work efficiency.
It will be evident to those skilled in the art that the invention is not limited to the details of the foregoing illustrative embodiments, and that the present invention may be embodied in other specific forms without departing from the spirit or essential attributes thereof. The present embodiments are therefore to be considered in all respects as illustrative and not restrictive, the scope of the invention being indicated by the appended claims rather than by the foregoing description, and all changes which come within the meaning and range of equivalency of the claims are therefore intended to be embraced therein. Any reference sign in a claim should not be construed as limiting the claim concerned.
Claims (8)
1. A screw surface rapid electroplating process is characterized by comprising the following steps: step one, chemical degreasing: adding the screw into hot alkali solution, and removing oil stains on the surface of the screw through saponification and emulsification of the hot alkali solution on oil; step two, hot water washing: adding hot water into an ultrasonic cleaning machine, and then adding the screw rod after oil removal into the ultrasonic cleaning machine for cleaning to remove impurities on the surface of the screw rod; step three, electroplating: putting the cleaned screw into a galvanizing solution, connecting the screw with a power supply, and converting zinc ions in the electroplating solution into simple substance zinc to cover the surface of the screw through oxidation-reduction reaction; step four, cleaning and drying: and (4) placing the galvanized screw into clear water to be cleaned once, taking out the screw after cleaning, and drying and storing.
2. The screw surface rapid plating process according to claim 1, characterized in that the zinc plating solution is an alkaline zincate plating solution.
3. The screw surface rapid plating process and the device thereof according to claim 1, characterized in that the temperature of the galvanizing solution is 0-50 ℃.
4. The device for the screw rod surface rapid electroplating process according to any one of claims 1 to 3, which comprises an electroplating box (1), and is characterized in that a power supply (2) is installed on the outer wall of the right side of the electroplating box (1), an anode rod (3) is installed on the inner wall of the right side of the electroplating box (1), the anode rod (3) is electrically connected with the power supply (2) through a first lead (4), a workpiece loading mechanism (6) extending into the electroplating box (1) is installed on the left side of the electroplating box, a hydraulic cylinder (7) is installed on the workpiece loading mechanism (6), a telescopic rod of the hydraulic cylinder (7) is connected with a mounting sleeve (8), the mounting sleeve (8) is made of an insulating material, an electrode plate (9) is installed inside the mounting sleeve (8), and the electrode plate (9) is electrically connected with the power supply (2) through a second lead (5), a plurality of first springs (10) with the inside bottom elastic connection of installation cover (8) are installed to the bottom of electrode slice (9), two clamping device (12) are installed in installation cover (8) to the upside of electrode slice (9), clamping device (12) include: splint (121) and second spring (122), splint (121) are through the inner wall elastic connection of a plurality of second springs (122) and installation cover (8), two install between clamping device (12) and extend to installation cover (8) outside screw rod (11), the bottom and the electrode slice (9) of screw rod (11) are laminated mutually.
5. The screw surface rapid plating process and the device thereof according to claim 4, characterized in that the power supply (2) is a DC power supply.
6. The screw surface rapid plating process and the device thereof according to claim 4, wherein the upper mechanism (6) comprises: step motor (601), action wheel (602), follow driving wheel (603), drive belt (604), pivot (605) and eccentric carousel (606), step motor (601) are fixed in the left side of electroplating case (1), install action wheel (602) on the output shaft of step motor (601), follow driving wheel (603) are installed to the top of action wheel (602), it is connected with action wheel (602) rotation to follow driving wheel (603) through drive belt (604), install on pivot (605) from driving wheel (603), pivot (605) extend to electroplating case (1) in link to each other with eccentric carousel (606), pivot (605) are connected with electroplating case (1) rotation through the bearing, install pneumatic cylinder (7) on eccentric carousel (606).
7. The screw surface rapid plating process and the device thereof according to claim 6, characterized in that the stepping motor (601) rotates 180 degrees each time.
8. The screw surface rapid plating process and the device thereof according to claim 6, wherein the diameter ratio of the driving wheel (602) and the driven wheel (603) is 1: 1.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202110897952.8A CN113584536A (en) | 2021-08-05 | 2021-08-05 | Screw surface rapid electroplating process and device thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202110897952.8A CN113584536A (en) | 2021-08-05 | 2021-08-05 | Screw surface rapid electroplating process and device thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN113584536A true CN113584536A (en) | 2021-11-02 |
Family
ID=78255628
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202110897952.8A Pending CN113584536A (en) | 2021-08-05 | 2021-08-05 | Screw surface rapid electroplating process and device thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN113584536A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114752989A (en) * | 2022-03-01 | 2022-07-15 | 江苏江航智飞机发动机部件研究院有限公司 | Precise electrolytic machining method for titanium alloy screws |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20190321861A1 (en) * | 2018-04-20 | 2019-10-24 | Applied Materials, Inc. | Cleaning components and methods in a plating system |
| CN210420220U (en) * | 2019-10-01 | 2020-04-28 | 鄱阳县骏锐渔具有限公司 | Fishhook production is with electroplating device |
| CN111394762A (en) * | 2020-05-08 | 2020-07-10 | 贵阳白云中航紧固件有限公司 | Automatic bolt electroplating device and electroplating method |
| CN212293780U (en) * | 2020-03-20 | 2021-01-05 | 杭州宏特粉沫镀锌有限公司 | Galvanizing device for hardware processing |
-
2021
- 2021-08-05 CN CN202110897952.8A patent/CN113584536A/en active Pending
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20190321861A1 (en) * | 2018-04-20 | 2019-10-24 | Applied Materials, Inc. | Cleaning components and methods in a plating system |
| CN210420220U (en) * | 2019-10-01 | 2020-04-28 | 鄱阳县骏锐渔具有限公司 | Fishhook production is with electroplating device |
| CN212293780U (en) * | 2020-03-20 | 2021-01-05 | 杭州宏特粉沫镀锌有限公司 | Galvanizing device for hardware processing |
| CN111394762A (en) * | 2020-05-08 | 2020-07-10 | 贵阳白云中航紧固件有限公司 | Automatic bolt electroplating device and electroplating method |
Non-Patent Citations (2)
| Title |
|---|
| 上海市电镀协会: "《实用电镀技术指南》", 31 March 2019, 上海科学普及出版社, pages: 62 * |
| 中国铁道科学研究院桥梁加固技术研究组: "《铁路桥梁预应力碳纤维板抗弯加固技术》", 30 June 2017, 中国铁道出版社, pages: 82 - 83 * |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114752989A (en) * | 2022-03-01 | 2022-07-15 | 江苏江航智飞机发动机部件研究院有限公司 | Precise electrolytic machining method for titanium alloy screws |
| CN114752989B (en) * | 2022-03-01 | 2024-01-02 | 江苏江航智飞机发动机部件研究院有限公司 | A precision electrolytic machining method for titanium alloy screws |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| KR20190039284A (en) | Electroplating equipment for small parts | |
| CN1442516A (en) | Rolling hanging type electroplating method and its rotating electroplating hanging device | |
| CN107779938A (en) | Full automatic plating machine and its electroplating technology | |
| CN214901461U (en) | PCB circuit board electroplating device | |
| CN114645309B (en) | Aluminum alloy handle stand surface coloring plating treatment device for exercise bicycle | |
| CN204661847U (en) | A kind of strong current cathode rotary formula electroplanting device | |
| CN213680850U (en) | Tinning stack of tinned wire processing usefulness | |
| CN210341114U (en) | Full-automatic electroplating equipment | |
| CN219490192U (en) | Nickel coating thickening device in diamond wire electroplating equipment | |
| CN218115647U (en) | Electroplating processing device with appointed hanging point | |
| CN217600881U (en) | High-efficient silver-plating device | |
| CN215163281U (en) | Plating bath stirring device | |
| CN213772255U (en) | Energy-saving environment-friendly electroplating device | |
| CN214830745U (en) | A semiconductor chip electroplating device | |
| KR100797329B1 (en) | Film removal device of anode for steel plate electroplating | |
| CN218321720U (en) | Automobile parts evenly electroplates carrier | |
| CN210560862U (en) | Device for electroplating electronic element | |
| CN209555386U (en) | A kind of novel automatic surface processing device | |
| CN112376107A (en) | High-efficiency electroplating device and method for small parts | |
| CN221267436U (en) | Conductive metal film water electrolytic plating filter element cleaning device | |
| CN215366039U (en) | Electroplating device for uniformity of automobile parts | |
| CN222205549U (en) | Metal surface anticorrosion treatment device | |
| CN114959855B (en) | Machining device applied to hardware electroplating | |
| CN211471606U (en) | Electronic product plated item platform | |
| CN211339725U (en) | Electroplating equipment is used in nut processing |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WD01 | Invention patent application deemed withdrawn after publication | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20211102 |