CN113478020A - Automatic chamfering device for end face of large pipeline - Google Patents
Automatic chamfering device for end face of large pipeline Download PDFInfo
- Publication number
- CN113478020A CN113478020A CN202111033178.2A CN202111033178A CN113478020A CN 113478020 A CN113478020 A CN 113478020A CN 202111033178 A CN202111033178 A CN 202111033178A CN 113478020 A CN113478020 A CN 113478020A
- Authority
- CN
- China
- Prior art keywords
- mounting
- groove
- transmission
- pipeline
- fixed mounting
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000003754 machining Methods 0.000 claims abstract description 17
- 230000005540 biological transmission Effects 0.000 claims description 92
- 238000009434 installation Methods 0.000 claims description 20
- 230000000694 effects Effects 0.000 claims description 12
- 238000010030 laminating Methods 0.000 claims description 6
- 230000000149 penetrating effect Effects 0.000 claims description 2
- 244000309464 bull Species 0.000 description 10
- 230000013011 mating Effects 0.000 description 5
- 238000000034 method Methods 0.000 description 5
- 239000007858 starting material Substances 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 210000001503 joint Anatomy 0.000 description 1
- 238000003801 milling Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000003032 molecular docking Methods 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23D—PLANING; SLOTTING; SHEARING; BROACHING; SAWING; FILING; SCRAPING; LIKE OPERATIONS FOR WORKING METAL BY REMOVING MATERIAL, NOT OTHERWISE PROVIDED FOR
- B23D79/00—Methods, machines, or devices not covered elsewhere, for working metal by removal of material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q1/00—Members which are comprised in the general build-up of a form of machine, particularly relatively large fixed members
- B23Q1/25—Movable or adjustable work or tool supports
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q11/00—Accessories fitted to machine tools for keeping tools or parts of the machine in good working condition or for cooling work; Safety devices specially combined with or arranged in, or specially adapted for use in connection with, machine tools
- B23Q11/0042—Devices for removing chips
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q3/00—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine
- B23Q3/02—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine for mounting on a work-table, tool-slide, or analogous part
- B23Q3/06—Work-clamping means
- B23Q3/062—Work-clamping means adapted for holding workpieces having a special form or being made from a special material
- B23Q3/064—Work-clamping means adapted for holding workpieces having a special form or being made from a special material for holding elongated workpieces, e.g. pipes, bars or profiles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q7/00—Arrangements for handling work specially combined with or arranged in, or specially adapted for use in connection with, machine tools, e.g. for conveying, loading, positioning, discharging, sorting
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Turning (AREA)
Abstract
The invention relates to the technical field of mechanical equipment, in particular to an automatic chamfering device for end faces of large pipelines, which comprises a workbench and a side position support, wherein movable wheels are respectively rotatably installed at the lower end of the side position support, a connecting matching groove is formed in one end, close to the side position support, of the workbench, the connecting matching groove is provided with the side position support in an extending mode through a second machining assembly, and the upper end of the side position support is fixedly provided with the second machining assembly. The time required for chamfering is greatly shortened.
Description
Technical Field
The invention relates to the technical field of mechanical equipment, in particular to an automatic chamfering device for an end face of a large pipeline.
Background
The application range of pipeline is extensive among the prior art, it is better stable when in order to make the pipeline use or install, thereby need carry out chamfer processing at the terminal surface of pipeline, wherein just need use chamfering equipment to process the terminal surface of pipeline, thereby current chamfering equipment need the manual work to carry out the chamfer operation when processing man-hour in the face of large-scale pipeline chamfer, the effect when having led to add the lower problem of processing efficiency and chamfer also can't guarantee, and current chamfering equipment can not carry out the simultaneous processing on both sides when carrying out the chamfer, thereby it is loaded down with trivial details to need to process many times and lead to the chamfer flow.
Disclosure of Invention
Technical problem to be solved
Aiming at the defects of the prior art, the invention provides an automatic chamfering device for the end face of a large pipeline, which solves the problems that the processing efficiency of the large pipeline is low and the processing quality cannot be ensured and the problem that the existing equipment is complicated in chamfering processing.
(II) technical scheme
In order to achieve the purpose, the invention adopts the technical scheme that:
an automatic chamfering device for end faces of large pipelines comprises a workbench and a side position support, wherein movable wheels are respectively rotatably mounted at the lower end of the side position support, a connecting matching groove is formed in one end, close to the side position support, of the workbench, the side position support is installed in the connecting matching groove in an extending mode through a second processing assembly, a second processing assembly is fixedly installed at the upper end of the side position support, a first processing assembly is fixedly installed at one end, far away from the side position support, of the upper surface of the workbench, a collecting groove is fixedly installed in each of the inner sides of the first processing assembly and the second processing assembly, a telescopic sleeve rod and an installation shell are respectively and fixedly installed in the middle of the upper surface of the workbench, the telescopic sleeve rod is fixedly installed at one end of the pipeline placing groove through the upper surface of a supporting spring, the installation shell is fixedly installed at the other end of the pipeline placing groove through the upper end of a tooth installation column, and a transmission installation plate is integrally arranged on one side of the pipeline placing groove, the surface of the transmission mounting plate is fixedly provided with a transmission assembly, and the upper surface of the pipeline placing groove is provided with a processing pipeline.
As preferred, the inside movable transmission groove of having seted up of installation shell, the tooth erection column is installed to the spacing installation in inside one side of movable transmission groove, the inside opposite side of movable transmission groove rotates and installs the meshing gear, the meshing gear upper end is rotated and is installed the transmission bull stick, transmission bull stick and meshing gear installation axle carry out the transmission through the drive belt and connect, the transmission bull stick runs through installation shell fixed mounting and has control knob, the inboard fixed mounting of side position support has the connection to extend the post, connect and extend the spacing activity setting of post and connect inside the mating groove, just connect and extend post through connection mating groove fixed mounting and have the control handle.
As preferred, drive assembly is including subassembly bracing piece and motor, motor fixed mounting is on the surface of transmission mounting panel, the subassembly bracing piece is equipped with two and fixed mounting respectively at workstation upper surface both ends, transmission mounting panel surface both ends fixed mounting respectively has the transmission shaft mounting bracket, the inside rotation of transmission shaft mounting bracket installs steering transmission shaft.
Preferably, the steering transmission shaft body and the motor output end are provided with helical gears and are meshed for transmission, the two ends of the steering transmission shaft body are fixedly provided with transmission processing pipeline rotating pipelines to rotate, the end parts of the two ends of the steering transmission shaft are rotatably provided with side position mounting plates, and each side position mounting plate is movably mounted on one side of the rod body of the component supporting rod respectively.
Preferably, the first processing assembly comprises a first mounting plate, a first limiting groove is formed in the plate body of the first mounting plate in a penetrating mode, the first limiting groove is longer than a second limiting groove in length, a first tool plate is slidably mounted in the first limiting groove, and a first processing cutter head is fixedly mounted at the inner end of the first tool plate through a bolt.
As preferred, the surface terminal surface of first processing tool bit knife face upwards and laminating processing pipeline, the inboard a week of first mounting panel plate body fixed mounting respectively has a plurality of L type loop bars, every the inside one end that is cavity and inside fixed mounting have the spring of L type loop bar, every the equal fixed mounting of the spring other end has the extension rod.
Preferably, every equal spacing activity of extension rod sets up inside L type loop bar, every the equal fixed mounting of extension rod tip has arc limiting plate, every equal spacing laminating processing pipeline inner ring of arc limiting plate.
As preferred, the second processing subassembly is including the second mounting panel, second mounting panel body runs through and has seted up the inside slidable mounting of second spacing groove and have the second tool plate, there is the second processing tool bit second tool plate inner through bolt fixed mounting, just the second processing tool bit knife face is downward and is located the inner ring of processing pipeline, the inboard lower extreme fixed mounting of second mounting panel body has the location arc, another location arc is installed through the rotation of upset pivot to the location arc.
Preferably, two be provided with the cooperation buckle between the location arc, every expansion mounting groove has all been seted up to location arc inner wall, every the inside one end of expansion mounting groove all rotates installs the upset bracing piece, every equal fixed mounting of upset bracing piece pole body has the arc to extend the board, every the arc extends board and corresponds arc draw-in groove and alternates clearance fit.
As preferred, every correspond the equal fixed mounting of arc draw-in groove and keep away from the one end of upset bracing piece, every inside extension mounting groove the equal rotation of upset bracing piece pole body tip installs spacing gyro wheel, every spacing gyro wheel all carries out spacing cooperation, every with the surface of processing pipeline the equal fixed mounting of first worker type board and second worker type board outer end has screw-thread fit board, every the equal fixed mounting of lower extreme has lead screw mounting bracket, per two on the screw-thread fit board rotate between the lead screw mounting bracket and install control lead screw, every control lead screw and corresponding screw-thread fit board carry out screw thread transmission.
Compared with the prior art, the invention has the following beneficial effects:
1. thereby drive through pull control handle and connect the extension post and carry out the activity adjustment inside connecting the cooperation groove, and the cooperation loose wheel realizes the control to length, thereby can avoid leading to unable chamfer processing because of the pipeline length difference, make this device adaptability promote thereupon, rotate the transmission bull stick through using control knob, and through utilizing transmission bull stick and meshing gear installation axle to carry out the transmission through the drive belt, thereby realize that meshing gear drives the tooth erection column and carries out activity from top to bottom and make the pipeline standing groove carry out position adjustment from top to bottom and through flexible loop bar through the one end of supporting spring fixed surface mounting in the pipeline standing groove make it more stable when adjusting.
2. Can realize rotating the processing pipeline through the transmission subassembly, and cooperate first processing subassembly and second processing subassembly to carry out the chamfer processing to the pipeline, utilize afterwards to turn to transmission shaft axle body and motor output end to all be provided with the helical gear and mesh the transmission through starter motor, make steering transmission shaft rotate, later drive both sides pipeline through steering transmission shaft and rotate the wheel and make the processing pipeline rotate, through every side position mounting panel respectively movable mounting make it carry out when adjusting from top to bottom at subassembly bracing piece pole body also can carry out normal transmission operation.
3. One end of a machined pipeline can be fixed through the first machining assembly, and because the positions of two side end faces to be machined are different when the pipelines are in butt joint, chamfering operation with required effects can be simultaneously carried out on the two end faces of a single pipeline through matching with the second machining assembly; the surface terminal surface through first processing tool bit knife face upwards and laminating processing pipeline during the use to the realization carries out the chamfer to the surface of processing pipeline, and utilizes spring mounting to have the extension rod through L type cover rod, makes the extension rod drive the arc limiting plate and carries on spacingly to processing pipeline inner wall, prevents to take place not hard up the problem appearance that drops when adding man-hour.
4. The other end face of the machined pipeline can be correspondingly chamfered through the second machining assembly, so that chamfering on two sides can be finished at one time, and the tool bit can be adjusted through the first machining assembly and the second machining assembly, so that the pipe orifice of the pipeline, which can be adapted by the device, is greatly increased, the corresponding adjustment and replacement can be carried out according to requirements, the intensity in machining is greatly reduced, the device can face different pipelines when in use, and the operation is convenient and fast in machining; during the use, it makes and to accomplish the cooperation pipeline terminal surface and adjust to alternate clearance fit through arc extension board and corresponding arc draw-in groove, and all rotate through upset bracing piece pole body tip and install spacing gyro wheel and make man-hour more stable, and utilize arc extension board and corresponding arc draw-in groove to alternate clearance fit and realize placing the pipeline earlier and spacing it again, and carry out the screw drive through control lead screw and corresponding screw fit board when using and realize highly adjusting first industrial board and second industrial board, thereby satisfy the personal required tool bit adjustment that corresponds that carries on.
Drawings
FIG. 1 is a schematic view of the overall structure of an automatic chamfering device for large pipe end faces according to the present invention;
FIG. 2 is a schematic rear view of an automatic chamfering apparatus for large pipe end faces according to the present invention;
FIG. 3 is a schematic view of a part of the structure of an automatic chamfering device for large pipe end faces according to the present invention;
FIG. 4 is a schematic top view of a part of an automatic chamfering apparatus for large pipe end faces according to the present invention;
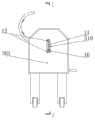
FIG. 5 is a schematic cross-sectional view taken along line A-A in FIG. 5 of an automatic chamfering apparatus for large pipe end faces according to the present invention;
FIG. 6 is a schematic cross-sectional view taken along line B-B in FIG. 5 of an automatic chamfering apparatus for large pipe end faces according to the present invention;
FIG. 7 is another schematic structural diagram of an automatic chamfering apparatus for large pipe end faces according to the present invention;
FIG. 8 is an enlarged schematic structural view of the automatic chamfering apparatus for large pipe end faces of the present invention at the position A in FIG. 7;
FIG. 9 is a schematic side view of another part of an automatic chamfering apparatus for large pipe end faces according to the present invention;
fig. 10 is a schematic cross-sectional view at C-C in fig. 9 of an automatic chamfering apparatus for an end surface of a large pipe according to the present invention.
In the figure: 1. a work table; 2. a first processing assembly; 201. a first mounting plate; 202. an arc limiting plate; 203. an extension rod; 204. an L-shaped loop bar; 205. a first machining tool bit; 206. a first tooling plate; 207. a first limit groove; 3. a second processing assembly; 301. a second mounting plate; 302. a second tooling plate; 303. connecting the extension column; 304. a second machining tool bit; 305. matching with a buckle; 306. positioning the arc-shaped plate; 307. turning over the rotating shaft; 308. expanding the mounting groove; 3081. an arc-shaped clamping groove; 3082. an arc-shaped extension plate; 3083. turning over the supporting rod; 3084. limiting the idler wheel; 309. a control grip; 310. a second limit groove; 4. a transmission assembly; 401. an assembly support rod; 402. a side position mounting plate; 403. a steering transmission shaft; 404. a motor; 405. a helical gear; 406. a transmission shaft mounting bracket; 407. a pipe running wheel; 5. collecting tank; 6. a lateral bracket; 7. a pipeline placing groove; 8. installing a shell; 9. a transmission mounting plate; 10. a movable wheel; 11. controlling the screw rod; 12. a lead screw mounting rack; 13. connecting the matching grooves; 14. a support spring; 15. a telescopic loop bar; 16. a screw-fit plate; 17. a control knob; 18. a tooth mounting post; 19. a movable transmission groove; 20. a transmission rotating rod; 21. a transmission belt; 22. engaging the gear.
Detailed Description
The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the embodiments of the present invention, and it is obvious that the described embodiments are only a part of the embodiments of the present invention, and not all of the embodiments. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
Examples
As shown in fig. 1-10, an automatic chamfering device for end faces of large pipelines comprises a workbench 1 and a side bracket 6, wherein the lower end of the side bracket 6 is respectively rotatably provided with a movable wheel 10, one end of the workbench 1 close to the side bracket 6 is provided with a connecting matching groove 13, the connecting matching groove 13 is provided with the side bracket 6 through a second processing component 3 in an extending way, the upper end of the side bracket 6 is fixedly provided with a second processing component 3, one end of the upper surface of the workbench 1 far away from the side bracket 6 is fixedly provided with a first processing component 2, the inner sides of the first processing component 2 and the second processing component 3 are both fixedly provided with a collecting groove 5, the middle part of the upper surface of the workbench 1 is respectively and fixedly provided with a telescopic loop bar 15 and an installation shell 8, the telescopic loop bar 15 is fixedly arranged at one end of the pipeline placing groove 7 through the upper surface of a supporting spring 14, the installation shell 8 is fixedly arranged at the other end of the pipeline placing groove 7 through the upper end of a tooth installation column 18, the transmission mounting plate 9 is arranged on one side of the pipeline placing groove 7 in an integrated mode, the transmission assembly 4 is fixedly mounted on the surface of the transmission mounting plate 9, and a machining pipeline is arranged on the upper surface of the pipeline placing groove 7.
Through the technical scheme, when in use, the distance between the side position bracket 6 and the workbench 1 is firstly adjusted according to the length of the pipeline, then the pipeline to be processed is placed on the lower surface of the pipeline placing groove 7, then the height is adjusted according to the size of the pipeline and adjusted to the processing position, after the processing, the first processing component 2 is firstly used for supporting and limiting the inner ring at one end of the processed pipeline, then the second processing component 3 is used for supporting and limiting the other end of the processed pipeline on the outer ring, the distance between the corresponding first and second milling heads 205 and 304 and the end surface of the pipe can be controlled and adjusted after the support limit, thereby reuse transmission assembly 4 after the completion and rotate the processing pipeline to cooperate first processing subassembly 2 and second processing subassembly 3 to process, add man-hour and still utilize collecting vat 5 to collect the sweeps that produce man-hour.
In this embodiment, installation shell 8 has inside offered movable transmission groove 19, the inside spacing tooth erection column 18 of installing in one side of movable transmission groove 19, the inside opposite side of movable transmission groove 19 is rotated and is installed meshing gear 22, meshing gear 22 upper end is rotated and is installed transmission bull stick 20, transmission bull stick 20 and meshing gear 22 installation axle carry out the transmission through drive belt 21 and connect, transmission bull stick 20 runs through installation shell 8 fixed mounting and has control knob 17, the inboard fixed mounting of side position support 6 has the connection to extend post 303, connect and extend the spacing activity of post 303 and set up inside connecting mating grooves 13, and connect and extend post 303 through connection mating grooves 13 fixed mounting and have control handle 309. Thereby drive through pull control handle 309 and connect extension post 303 and carry out the activity adjustment inside connecting mating groove 13, and cooperation loose wheel 10 realizes the control to length, thereby can avoid leading to unable chamfer processing because of the pipeline length difference, make this device adaptability promote thereupon, rotate transmission bull stick 20 through using control knob 17, and through utilizing transmission bull stick 20 and meshing gear 22 installation axle to carry out the transmission through drive belt 21, thereby realize that meshing gear 22 drives tooth erection column 18 and carries out the activity about and make pipeline standing groove 7 carry out position adjustment from top to bottom and make it more stable when adjusting through telescopic sleeve pole 15 through the one end of supporting spring 14 upper surface fixed mounting in pipeline standing groove 7.
It should be noted that, transmission assembly 4 is including subassembly bracing piece 401 and motor 404, motor 404 fixed mounting is on the surface of transmission mounting panel 9, subassembly bracing piece 401 is equipped with two and respectively fixed mounting at workstation 1 upper surface both ends, transmission mounting panel 9 surface both ends respectively fixed mounting have transmission shaft mounting bracket 406, transmission shaft mounting bracket 406 is inside to be rotated and to be installed steering transmission shaft 403, steering transmission shaft 403 shaft body and motor 404 output all are provided with helical gear 405 and mesh the transmission, steering transmission shaft 403 shaft body both ends all fixed mounting have transmission processing pipeline pivoted pipeline to rotate wheel 407, steering transmission shaft 403 both ends tip all rotates and installs side position mounting panel 402, every side position mounting panel 402 is movable mounting respectively in subassembly bracing piece 401 pole body one side. Can realize rotating the processing pipeline through transmission assembly 4, and cooperate first processing assembly 2 and second processing assembly 3 to carry out the chamfer processing to the pipeline, utilize afterwards to turn to transmission shaft 403 shaft body and motor 404 output through starter motor 404 and all be provided with helical gear 405 and mesh the transmission, make to turn to transmission shaft 403 to rotate, later drive both sides pipeline through turning to transmission shaft 403 and rotate wheel 407 and make the processing pipeline rotate, through every side position mounting panel 402 respectively movable mounting make it carry out from top to bottom when adjusting at subassembly bracing piece 401 pole body also can carry out normal transmission operation.
When specifically setting up, first processing subassembly 2 is including first mounting panel 201, and first mounting panel 201 board body runs through and has seted up first spacing groove 207, and first spacing groove 207 is seted up length and is longer than second spacing groove 310, and the inside slidable mounting of first spacing groove 207 has first board 206, and first board 206 is the inner first processing tool bit 205 of having through bolt fixed mounting, and first processing tool bit 205 knife face is upwards just laminating the surface terminal surface of processing pipeline. Can fix the one end of processing pipeline through first processing subassembly 2 to the position that the both sides terminal surface needs to be processed is different when docking because of the pipeline, thereby it carries out the chamfer operation that required effect to carry out the both ends face to single pipeline simultaneously to realize through cooperation second processing subassembly 3, compare with prior art and need not to carry out a lot of processing and carry out the change of tool bit when carrying out multiaspect processing, thereby reduce single pipeline and add man-hour required flow, shorten chamfer processing required time greatly.
It can be understood that in this application, the inboard a week of first mounting panel 201 board body is fixed mounting respectively has a plurality of L type loop bars 204, and every L type loop bar 204 is inside to be the one end of cavity and inside fixed mounting having the spring, and the equal fixed mounting of every spring other end has extension rod 203, and the equal spacing activity of every extension rod 203 sets up inside L type loop bar 204, and the equal fixed mounting of every extension rod 203 tip has arc limiting plate 202, and the equal spacing laminating of every arc limiting plate 202 processes the pipeline inner ring. Go up and laminate the surface terminal surface of processing pipeline through first processing tool bit 205 knife face during the use to the realization carries out the chamfer to the surface of processing pipeline, and utilizes spring mounting to have extension rod 203 through L type cap rod 204, makes extension rod 203 drive arc limiting plate 202 carry on spacingly to processing pipeline inner wall, prevents to take place not hard up the problem appearance that drops when adding man-hour.
When specifically setting up, second processing subassembly 3 is including second mounting panel 301, second mounting panel 301 board body runs through and has seted up second spacing groove 310 and the inside slidable mounting of second spacing groove 310 has second tool plate 302, second tool plate 302 is inner has second processing tool bit 304 through bolt fixed mounting, and second processing tool bit 304 knife face is downward and be located the inner ring of processing pipeline, the inboard lower extreme fixed mounting of second mounting panel 301 board body has location arc 306, location arc 306 rotates through upset pivot 307 and installs another location arc 306, be provided with cooperation buckle 305 between two location arcs 306, extension mounting groove 308 has all been seted up to every location arc 306 inner wall, the inside one end of every extension mounting groove 308 all rotates installs upset bracing piece 3083. Can carry out the chamfer processing that corresponds to another terminal surface of processing pipeline through second processing subassembly 3 to realize once accomplishing two sides chamfer, and all can carry out the adjustment to the tool bit through first processing subassembly 2 and second processing subassembly 3, thereby realize the pipeline mouth of pipe greatly increased that this device can adapt to, and can carry out the adjustment change that corresponds according to the demand, greatly reduced adds intensity man-hour, make this device can face different pipelines and add the simple operation man-hour when using.
Wherein, every upset bracing piece 3083 pole body equal fixed mounting has arc extending plate 3082, every arc extending plate 3082 alternates clearance fit with corresponding arc draw-in groove 3081, every corresponding arc draw-in groove 3081 equal fixed mounting is in the inside one end of keeping away from upset bracing piece 3083 of extension mounting groove 308, every upset bracing piece 3083 pole body tip all rotates and installs spacing gyro wheel 3084, every spacing gyro wheel 3084 all carries out limit fit with the surface of processing pipeline, every first industry board 206 and the equal fixed mounting of second industry board 302 outer end have screw-thread fit plate 16, the equal fixed mounting of lower extreme has lead screw mounting bracket 12 on every screw-thread fit plate 16, rotate between per two lead screw mounting bracket 12 and install control lead screw 11, every control lead screw 11 carries out screw-thread transmission with corresponding screw-thread fit plate 16. During the use, it makes can accomplish the cooperation pipeline terminal surface and adjust to alternate clearance fit through arc extending plate 3082 and corresponding arc draw-in groove 3081, and all rotate to install spacing gyro wheel 3084 through upset bracing piece 3083 pole body tip and make to add man-hour more stable, and utilize arc extending plate 3082 and corresponding arc draw-in groove 3081 to alternate clearance fit and realize can placing the pipeline earlier and spacing it again, and carry out the screw transmission through control lead screw 11 and corresponding screw-thread fit plate 16 when using and realize highly adjusting first worker's board 206 and second worker's board 302, thereby satisfy the personal required tool bit adjustment that corresponds that carries out.
The working principle of the automatic chamfering device for the end face of the large pipeline is as follows:
during the use at first, according to the distance between pipeline length adjustment side position support 6 and the workstation 1, place the pipeline of required processing at pipeline standing groove 7 lower surface afterwards, later carry out height control and adjust to the processing position according to the size of pipeline, it is spacing to use earlier the inner ring of processing pipeline one end to support first processing subassembly 2 after accomplishing, it is spacing to utilize the second processing subassembly 3 to carry out the support of outer lane with it later on, can control the adjustment to the distance of first processing tool bit 205 and second processing tool bit 304 and the pipeline end face that corresponds after supporting spacingly, thereby reuse drive assembly 4 and rotate the processing pipeline after accomplishing, and cooperate first processing subassembly 2 and second processing subassembly 3 to process, still utilize collecting vat 5 to collect the sweeps that produces man-hour during processing.
It should be noted that the specific model specification of the motor 404 is HF-SP 102K.
The foregoing shows and describes the general principles and broad features of the present invention and advantages thereof. It will be understood by those skilled in the art that the present invention is not limited to the embodiments described above, which are described in the specification and illustrated only to illustrate the principle of the present invention, but that various changes and modifications may be made therein without departing from the spirit and scope of the present invention, which fall within the scope of the invention as claimed. The scope of the invention is defined by the appended claims and equivalents thereof.
Claims (10)
1. The utility model provides an automatic chamfer device of large-scale pipeline terminal surface, includes workstation (1) and side position support (6), side position support (6) lower extreme rotates respectively and installs loose wheel (10), workstation (1) is close to the one end of side position support (6) and has seted up connection cooperation groove (13), its characterized in that: the side position support (6) is installed on the connecting matching groove (13) in an extending mode through the second machining component (3), the second machining component (3) is installed at the upper end of the side position support (6) in a fixed mode, the first machining component (2) is installed at one end, far away from the side position support (6), of the upper surface of the workbench (1), the collecting groove (5) is fixedly installed on the inner sides of the first machining component (2) and the second machining component (3), the middle portion of the upper surface of the workbench (1) is fixedly installed with the telescopic loop bar (15) and the installation shell (8) respectively, the telescopic loop bar (15) is fixedly installed at one end of the pipeline placing groove (7) through the upper surface of the supporting spring (14), the installation shell (8) is fixedly installed at the other end of the pipeline placing groove (7) through the upper end of the tooth installation column (18), and the transmission installation plate (9) is arranged on one side of the pipeline placing groove (7) in an integrated mode, the surface of the transmission mounting plate (9) is fixedly provided with a transmission assembly (4), and the upper surface of the pipeline placing groove (7) is provided with a processing pipeline.
2. The automatic chamfering device for the end faces of the large pipelines according to claim 1, wherein: a movable transmission groove (19) is arranged in the mounting shell (8), a tooth mounting column (18) is arranged on one side of the inner part of the movable transmission groove (19) in a limiting way, the other side in the movable transmission groove (19) is rotatably provided with a meshing gear (22), the upper end of the meshing gear (22) is rotatably provided with a transmission rotating rod (20), the transmission rotating rod (20) is in transmission connection with a mounting shaft of the meshing gear (22) through a transmission belt (21), the transmission rotating rod (20) is fixedly provided with a control knob (17) by penetrating through the mounting shell (8), the inner side of the side position bracket (6) is fixedly provided with a connecting extension column (303), the connecting extension column (303) is movably arranged in the connecting matching groove (13) in a limiting way, and the connection extension column (303) is fixedly provided with a control grip (309) through the connection matching groove (13).
3. The automatic chamfering device for the end faces of the large pipelines according to claim 1, wherein: drive assembly (4) is including subassembly bracing piece (401) and motor (404), motor (404) fixed mounting is on the surface of transmission mounting panel (9), subassembly bracing piece (401) are equipped with two and respectively fixed mounting at workstation (1) upper surface both ends, transmission mounting panel (9) surface both ends respectively fixed mounting have transmission shaft mounting bracket (406), transmission shaft mounting bracket (406) internal rotation installs steering transmission shaft (403).
4. The automatic chamfering device for the end faces of large pipes according to claim 3, wherein: turn to transmission shaft (403) shaft body and motor (404) output and all be provided with helical gear (405) and mesh the transmission, turn to equal fixed mounting in transmission shaft (403) shaft body both ends and have transmission processing pipeline pivoted pipeline to rotate wheel (407), turn to transmission shaft (403) both ends tip and all rotate and install side position mounting panel (402), every side position mounting panel (402) movable mounting respectively is in subassembly bracing piece (401) pole body one side.
5. The automatic chamfering device for the end faces of the large pipelines according to claim 1, wherein: first processing subassembly (2) is including first mounting panel (201), first mounting panel (201) shaft runs through and has seted up first spacing groove (207), length is longer than second spacing groove (310) in first spacing groove (207) seting up, first spacing groove (207) inside slidable mounting has first board (206), first board (206) the inner has first processing tool bit (205) through bolt fixed mounting.
6. The automatic chamfering device for the end faces of large pipes according to claim 5, wherein: first processing tool bit (205) knife face upwards and laminate the surface terminal surface of processing pipeline, the inboard a week of first mounting panel (201) body fixed mounting respectively has a plurality of L type loop bars (204), every L type loop bar (204) inside is the one end that cavity and inside fixed mounting have the spring, every the equal fixed mounting of the spring other end has extension rod (203).
7. The automatic chamfering device for the end faces of large pipes according to claim 6, wherein: every equal spacing activity of extension rod (203) sets up inside L type telescopic pole (204), every extension rod (203) equal fixed mounting in tip has arc limiting plate (202), every equal spacing laminating processing pipeline inner ring of arc limiting plate (202).
8. The automatic chamfering device for the end faces of large pipes according to claim 7, wherein: second processing subassembly (3) is including second mounting panel (301), second mounting panel (301) board body runs through to have seted up second spacing groove (310) and second spacing groove (310) inside slidable mounting has second worker's board (302), second worker's board (302) inner has second processing tool bit (304) through bolt fixed mounting, just second processing tool bit (304) knife face is down and is located the inner ring of processing pipeline, second mounting panel (301) inboard lower extreme fixed mounting of board body has location arc (306), location arc (306) rotate through upset pivot (307) and install another location arc (306).
9. The automatic chamfering device for the end faces of large pipes according to claim 8, wherein: two be provided with cooperation buckle (305), every between location arc (306) expansion mounting groove (308), every have all been seted up to location arc (306) inner wall expansion mounting groove (308) inside one end of expansion mounting groove (308) all rotates and installs upset bracing piece (3083), every equal fixed mounting of upset bracing piece (3083) pole body has arc to extend board (3082), every arc extends board (3082) and corresponds arc draw-in groove (3081) and alternates clearance fit.
10. The automatic chamfering device for the end faces of large pipes according to claim 9, wherein: every correspond the equal fixed mounting of arc draw-in groove (3081) and keep away from the one end of upset bracing piece (3083), every inside extension mounting groove (308) the upset bracing piece (3083) pole body tip all rotates and installs spacing gyro wheel (3084), every spacing gyro wheel (3084) all carries out limit fit with the surface of processing pipeline, every first worker's board (206) and the equal fixed mounting in second worker's board (302) outer end have screw-thread fit board (16), every the equal fixed mounting of lower extreme has lead screw mounting bracket (12), per two rotate between lead screw mounting bracket (12) and install control lead screw (11), every control lead screw (11) and corresponding screw-thread fit board (16) carry out screw-thread transmission.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111033178.2A CN113478020B (en) | 2021-09-03 | 2021-09-03 | Automatic chamfering device for end face of large pipeline |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111033178.2A CN113478020B (en) | 2021-09-03 | 2021-09-03 | Automatic chamfering device for end face of large pipeline |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN113478020A true CN113478020A (en) | 2021-10-08 |
| CN113478020B CN113478020B (en) | 2021-11-16 |
Family
ID=77947168
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202111033178.2A Active CN113478020B (en) | 2021-09-03 | 2021-09-03 | Automatic chamfering device for end face of large pipeline |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN113478020B (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116079547A (en) * | 2023-03-15 | 2023-05-09 | 青岛创力工具有限公司 | Medical grinding and retaining needle grinding wheel and manufacturing method thereof |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH07276205A (en) * | 1994-12-19 | 1995-10-24 | Bando Kiko Kk | Glass plate processing machine |
| KR20140142513A (en) * | 2013-06-04 | 2014-12-12 | 금오공과대학교 산학협력단 | Chamfering |
| CN206689541U (en) * | 2017-05-02 | 2017-12-01 | 江西森阳科技股份有限公司 | A kind of magnetic material automatic chamfering machine |
| CN111266957A (en) * | 2019-11-22 | 2020-06-12 | 广东鑫隆管业有限公司 | Port deburring device for production of reinforced concrete drain pipe |
| CN112372426A (en) * | 2020-01-03 | 2021-02-19 | 沈水文 | Pipeline chamfering and grinding control method |
| CN212946529U (en) * | 2020-07-27 | 2021-04-13 | 杭州铪威五金机械有限公司 | Hardware inside wall beveling machine |
| CN112720128A (en) * | 2020-12-28 | 2021-04-30 | 陈超 | Rubber pipeline processingequipment |
-
2021
- 2021-09-03 CN CN202111033178.2A patent/CN113478020B/en active Active
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH07276205A (en) * | 1994-12-19 | 1995-10-24 | Bando Kiko Kk | Glass plate processing machine |
| KR20140142513A (en) * | 2013-06-04 | 2014-12-12 | 금오공과대학교 산학협력단 | Chamfering |
| CN206689541U (en) * | 2017-05-02 | 2017-12-01 | 江西森阳科技股份有限公司 | A kind of magnetic material automatic chamfering machine |
| CN111266957A (en) * | 2019-11-22 | 2020-06-12 | 广东鑫隆管业有限公司 | Port deburring device for production of reinforced concrete drain pipe |
| CN112372426A (en) * | 2020-01-03 | 2021-02-19 | 沈水文 | Pipeline chamfering and grinding control method |
| CN212946529U (en) * | 2020-07-27 | 2021-04-13 | 杭州铪威五金机械有限公司 | Hardware inside wall beveling machine |
| CN112720128A (en) * | 2020-12-28 | 2021-04-30 | 陈超 | Rubber pipeline processingequipment |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116079547A (en) * | 2023-03-15 | 2023-05-09 | 青岛创力工具有限公司 | Medical grinding and retaining needle grinding wheel and manufacturing method thereof |
| CN116079547B (en) * | 2023-03-15 | 2023-11-07 | 青岛创力工具有限公司 | Medical grinding and retaining needle grinding wheel and manufacturing method thereof |
Also Published As
| Publication number | Publication date |
|---|---|
| CN113478020B (en) | 2021-11-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN114406591A (en) | Can convertible material rapid welding device | |
| CN113478020B (en) | Automatic chamfering device for end face of large pipeline | |
| CN113601197A (en) | CNC digit control machine tool rotary machining platform | |
| CN214921277U (en) | Welding device for thick steel plate of wind power tower | |
| CN214816757U (en) | Sand mould numerical control milling process frock clamp convenient to angle regulation | |
| CN117139743B (en) | Gear hobbing device for gear machining and machining method | |
| CN220838681U (en) | Welding fixture for white automobile body | |
| CN112719991A (en) | Multifunctional clamp for machine tool | |
| CN217493359U (en) | Linear guide rail drilling machine | |
| CN213053723U (en) | Spare part centre gripping fixing device that machining used | |
| CN211681095U (en) | A power head for CNC lathe | |
| CN220480450U (en) | Gear processing machine tool | |
| CN221088049U (en) | Frock clamp of adjustable accurate positioning | |
| CN221210121U (en) | Front fork outer tube reaming device | |
| CN222002433U (en) | Automatic change pipe jacking welding professional equipment | |
| CN223418367U (en) | A turning mechanism | |
| CN223313127U (en) | Angle-adjustable gear hobbing machine and gear | |
| CN207086979U (en) | Rig with support frame | |
| CN220051586U (en) | Auxiliary positioning device for mobile phone assembly | |
| CN221583925U (en) | Woodworking lathe tool mechanism with adjustable angle | |
| CN222806130U (en) | A drilling equipment for automobile parts | |
| CN222957787U (en) | Automatic double-station welding device | |
| CN218946993U (en) | Automobile steering knuckle key groove machining tool | |
| CN221269753U (en) | Auxiliary processing device for aluminum profile | |
| CN220943518U (en) | Gear part processing positioning structure |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |