Disclosure of Invention
In order to solve the technical problem, the application provides a full-automatic lens production and processing equipment.
In order to solve the technical problem, the following technical scheme is adopted in the application:
the full-automatic lens production and processing equipment comprises a rack, wherein a grinding device and a swinging device are arranged on the rack at intervals, the swinging device comprises a swinging mechanism arranged on the rack, a lifting mechanism connected to the driving end of the swinging mechanism and a pressing mechanism arranged on the lifting mechanism, the lifting mechanism is used for driving the pressing mechanism to be close to or far away from the grinding device, and the swinging mechanism is used for driving the lifting mechanism to swing so as to enable the pressing mechanism to swing relative to the grinding device;
the pressing mechanism comprises a connecting seat arranged on the lifting mechanism in a sliding mode, a lens absorbing group arranged on the connecting seat and used for absorbing lenses, and a lens jacking group arranged between the lifting mechanism driving end and the connecting seat, wherein the lens jacking group is used for driving the lens absorbing group to press towards the grinding device.
According to the full-automatic lens production and processing equipment, the lens jacking group comprises a fixed seat connected with the driving end of the lifting mechanism, a guide piece arranged between the connecting seat and the fixed seat and used for guiding, and a jacking air cylinder arranged between the fixed seat and the connecting seat and used for providing jacking potential energy.
According to the full-automatic lens production and processing equipment, the jacking cylinder is a needle-shaped cylinder, and an air pressure adjusting device for adjusting the pressure of the needle-shaped cylinder is connected to the needle-shaped cylinder.
Full-automatic lens production and processing equipment as above, lens absorb group including inhale press inner tube, activity butt in inhale the sucking disc of pressing the inner tube tip press the seat, overlap respectively and establish inhale press the inner tube with the clutch sleeve that the seat was pressed to the sucking disc, and locate on the connecting seat and with clutch sleeve connects's separation and reunion drive group, inhale the inside inner chamber that is equipped with and runs through of pressing the inner tube, the sucking disc press be equipped with on the seat with the hole of inhaling of inner chamber intercommunication, separation and reunion drive group is used for the drive clutch sleeve breaks away from or cup joints the seat is pressed to the sucking disc, sucking disc press seat up end to be equipped with inside sunken bell groove, it is equipped with and extends to inhale the inner tube lower extreme the top pressure needle in the bell groove.
According to the full-automatic lens production and processing equipment, the sucking disc pressing seat comprises a sleeving part and a sucking disc part, the sleeving part is arranged at the upper end of the sucking disc pressing seat and is used for being sleeved in the clutch sleeve, the sucking disc part is arranged at the lower end of the sucking disc part, an accommodating cavity which is inwards sunken and used for accommodating a lens is arranged on the lower end face of the sucking disc part, and the sucking hole penetrates through the sleeving part and the sucking disc part.
According to the full-automatic lens production and processing equipment, the inner wall of the clutch sleeve is provided with the inner tube sealing element which is in close contact with the suction pressure inner tube and the suction seat sealing element which is in close contact with the suction cup pressure seat, and a sealing cavity is formed among the clutch sleeve, the suction pressure inner tube and the suction cup pressure seat.
According to the full-automatic lens production and processing equipment, the clutch driving set comprises the clutch driving piece arranged on the connecting seat and the connecting rod set sleeved on the connecting seat in a penetrating manner, one end of the connecting rod set is connected with the driving end of the clutch driving piece, and the other end of the connecting rod set is connected with the clutch sleeve.
The full-automatic lens production and processing equipment comprises a swing driving part, a transmission assembly and a driving shaft, wherein the swing mechanism comprises a swing driving part, a transmission assembly and a driving shaft;
the transmission assembly comprises a driving wheel arranged on the driving end of the swinging driving piece, a driven wheel connected with the driving shaft, and a synchronous belt respectively sleeved with the driving wheel and the driven wheel;
the driving shaft is sleeved on the rack, one end of the driving shaft is connected with the driven wheel, and the other end of the driving shaft is connected with the lifting mechanism.
According to the full-automatic lens production and processing equipment, the lifting mechanism comprises a fixing plate connected with the driving end of the swing mechanism and a lifting driving piece arranged between the fixing plate and the connecting seat, and the lifting driving piece is used for driving the fixing plate to be close to or far away from the grinding device.
The full-automatic lens production and processing equipment further comprises an intelligent feeding and discharging system arranged on the rack, wherein the intelligent feeding and discharging system comprises a feeding and discharging device and a cleaning device which is arranged on one side of the feeding and discharging device and used for cleaning lenses;
the feeding and discharging device is used for feeding the lens to be processed and conveying the processed lens to the cleaning device for cleaning, and the feeding and discharging device is also used for discharging the cleaned lens.
Compared with the prior art, the beneficial effects of this application are as follows:
1. the application provides a full-automatic lens production and processing device, which comprises a grinding device for grinding lenses and a swinging device for driving the lenses to be ground, wherein the swinging device comprises a swinging mechanism, a lifting mechanism and a pressing mechanism, the pressing mechanism comprises a connecting seat, a lens suction group and a lens jacking group, when the device is used, the lenses are sucked by the lens suction group, the lenses sucked by the lens suction group are descended to the position of the grinding device through the lifting mechanism, then the lenses on the lens suction group are driven to press against the grinding device through the lens jacking group, the lenses are driven to swing along the grinding device through the swinging mechanism for processing, the device can firstly suck the lenses and then descend to the grinding position for grinding, the automation is improved, the lenses are not required to be manually placed, in addition, the device firstly descends the lenses through the lifting mechanism and then presses the lenses to the grinding device through the lens jacking group, play the buffering guard action, can avoid the lens to press to explode the damage.
2. The utility model provides a lens absorbs the group and presses the inner tube including inhaling, the sucking disc presses seat and clutch sleeve, absorb the group through the lens during use and absorb the lens, the lens that the sucking disc pressed the seat to go up the absorption drops to grinding mechanism counterbalance through elevating system and hold-down mechanism, drive clutch sleeve through separation and reunion drive group this moment and break away from the sucking disc and press the seat, make the sucking disc press seat and lens by the roof pressure at the pressure inner tube with grinding mechanism within a definite time, drive the lens through swing mechanism along grinding mechanism swing in order to process, this application can absorb the lens earlier, fall the grinding position with the lens again and grind, do not need the people to place the lens manually, and the operation is simple, and the automation is improved.
Drawings
In order to more clearly illustrate the technical solutions in the embodiments of the present application, the drawings used in the description of the embodiments will be briefly introduced below.
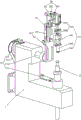
FIG. 1 is a schematic structural view of a fully automatic lens manufacturing apparatus according to the present invention.
Fig. 2 is a schematic structural diagram of a frame 1, a grinding device 2 and a swinging device 3 of the fully automatic lens production and processing equipment of the invention.
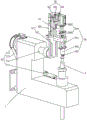
Fig. 3 is a schematic diagram of the state that the lifting mechanism 32 drives the lens pressing set 35, the connecting seat 33, and the lens sucking set 34 to descend to the position close to the grinding device 2 in the full-automatic lens producing and processing apparatus of the present invention.
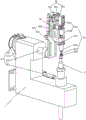
Fig. 4 is a schematic diagram of a state that the clutch driving unit 344 drives the clutch sleeve 343 to ascend and separate from the suction cup pressing base 342 after the lifting mechanism 32 drives the lens pressing unit 35, the connecting seat 33, and the lens sucking unit 34 to descend to a position close to the grinding device 2 in the full-automatic lens producing and processing apparatus of the present invention.
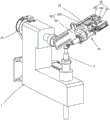
Fig. 5 is a schematic diagram of a state that the swing mechanism 31 drives the lifting mechanism 32 to swing when the full-automatic lens production and processing equipment of the present application is in operation.
Fig. 6 is a schematic diagram of another view angle of the swing mechanism 31 driving the lifting mechanism 32 to swing when the full-automatic lens production and processing equipment of the present application is in operation.
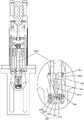
FIG. 7 is a schematic cross-sectional view of a pressing mechanism in the fully automatic lens manufacturing apparatus of the present invention.
Fig. 8 is a schematic cross-sectional view of the pressing mechanism in the fully automatic lens manufacturing apparatus of the present invention, and the clutch driving unit 344 drives the clutch sleeve 343 to ascend and separate from the suction cup pressing base 342.
Fig. 9 is an exploded view of the lifting mechanism and the pressing mechanism of the fully automatic lens manufacturing and processing apparatus of the present application.
Fig. 10 is a schematic structural diagram of the intelligent loading and unloading system of the present application.
Fig. 11 is a schematic structural view of the conveyance mechanism 53 in the embodiment of the present application.
Fig. 12 is a schematic structural diagram of the cleaning device 6, the loading station 50 and the pre-positioning device 7 in the embodiment of the application.
Fig. 13 is a schematic structural diagram of another view angle of the cleaning device 6, the loading station 50 and the pre-positioning device 7 in the embodiment of the application.
Detailed Description
As shown in fig. 1 to 13, a full-automatic lens production and processing apparatus includes a frame 1, a grinding device 2 and a swinging device 3 are disposed on the frame 1 at intervals, the swinging device 3 includes a swinging mechanism 31 disposed on the frame 1, a lifting mechanism 32 connected to a driving end of the swinging mechanism 31, and a pressing mechanism disposed on the lifting mechanism 32, the lifting mechanism 32 is configured to drive the pressing mechanism to approach or separate from the grinding device 2, and the swinging mechanism 31 is configured to drive the lifting mechanism 32 to swing so that the pressing mechanism swings relative to the grinding device 2; the pressing mechanism comprises a connecting seat 33 arranged on the lifting mechanism 32 in a sliding manner, a lens suction group 34 arranged on the connecting seat 33 and used for sucking the lens, and a lens jacking group 35 arranged between the driving end of the lifting mechanism 32 and the connecting seat 33, wherein the lens jacking group 35 is used for driving the lens suction group 34 to press towards the grinding device 2.
The application provides a full-automatic lens production and processing device, which comprises a grinding device for grinding lenses and a swinging device for driving the lenses to be ground, wherein the swinging device comprises a swinging mechanism, a lifting mechanism and a pressing mechanism, the pressing mechanism comprises a connecting seat, a lens suction group and a lens jacking group, when the device is used, the lenses are sucked by the lens suction group, the lenses sucked by the lens suction group are descended to the position of the grinding device through the lifting mechanism, then the lenses on the lens suction group are driven to press against the grinding device through the lens jacking group, the lenses are driven to swing along the grinding device through the swinging mechanism for processing, the device can firstly suck the lenses and then descend to the grinding position for grinding, the automation is improved, the lenses are not required to be manually placed, in addition, the device firstly descends the lenses through the lifting mechanism and then presses the lenses to the grinding device through the lens jacking group, play the buffering guard action, can avoid the lens to press to explode the damage.
Preferably, the lens pressing set 35 includes a fixing base 351 connected to the driving end of the lifting mechanism 32, a guiding member 352 disposed between the connecting base 33 and the fixing base 351 for guiding, and a pressing cylinder 353 disposed between the fixing base 351 and the connecting base 33 for providing pressing potential energy. The guide piece is a connecting rod sleeved on the connecting seat and is arranged in parallel to the sliding direction of the lens suction group, and the jacking cylinder is arranged to provide buffering assistance force so as to avoid direct pressing and explosion of the lens when the lens is driven to be pressed down by the lifting mechanism.
Preferably, the top pressure cylinder 353 is a needle-shaped cylinder, and the needle-shaped cylinder is connected with an air pressure adjusting device 4 for adjusting the pressure of the needle-shaped cylinder. To the lens of different thickness or specification, accessible atmospheric pressure adjusting device adjusts the pressure size that roof pressure cylinder drove the lens and press to grinder, improves intellectuality, protects the lens.
Preferably, the lens suction set 34 includes a suction/pressure inner tube 341, a suction cup pressing base 342 movably abutted to an end of the suction/pressure inner tube 341, a clutch sleeve 343 respectively sleeved on the suction/pressure inner tube 341 and the suction cup pressing base 342, and a clutch driving set 344 disposed on the connecting base 33 and connected to the clutch sleeve 343, wherein a through inner cavity 3410 is disposed inside the suction/pressure inner tube 341, a suction hole 3420 communicated with the inner cavity 3410 is disposed on the suction cup pressing base 342, the clutch driving set 344 is used for driving the clutch sleeve 343 to disengage or be sleeved on the suction cup pressing base 342, an inwardly recessed tapered groove 3421 is disposed on an upper end surface of the suction cup pressing base 342, and a pressing needle 3411 extending into the tapered groove 3421 is disposed at a lower end of the suction/pressure inner tube 341. The lens is sucked by the lens sucking group during use, the lens sucked on the sucker pressing seat descends to the position of the grinding device through the lifting mechanism, the lens is driven to abut against the grinding device through the lens ejecting group, the clutch sleeve is driven to separate from the sucker pressing seat 342 through the clutch driving group at the moment, so that the sucker pressing seat and the lens are pressed between the sucking inner tube and the grinding device by the ejecting pressure, the lens is driven to swing along the grinding device through the swinging mechanism to be processed, the lens can be sucked firstly in the application, the lens is then descended to the grinding position to be ground, and the lens is not required to be manually placed by a person. The application is the V type is personally submitted to the bell jar cross section, through the bell jar of impressing under the roof pressure needle to with the lens spacing grinding ware on roof pressure needle and grinder within a definite time, when grinding ware rotates, the sucking disc pressure seat rotates around the roof pressure needle, and the anthropomorphic dummy is manual to rotate around grinding the ware, makes the lens processing even.
Preferably, the suction cup holder 342 includes a sleeving part 3424 disposed at an upper end for sleeving in the clutch sleeve 343 and a suction cup part 3422 disposed at a lower end, an accommodating cavity 3425 recessed inwards for accommodating a lens is disposed on a lower end surface of the suction cup part 3422, and the suction hole 3420 penetrates through the sleeving part 3424 and the suction cup part 3422. The inner arc face through the holding cavity is used for fitting the arc face on the lens, prevent lens dislocation, influence the processing effect, the cover of the joint part is arranged in the clutch sleeve during use, make the lens absorb the vacuum inside the group, adsorb the lens firmly through the sucking disc portion, can avoid manual contact, under elevating system's drive, the lens descends to the grinding position, clutch drive group drive clutch sleeve rises this moment, the sucking disc presses the seat to lose clutch sleeve's effect, make the vacuum state contact, open grinding mechanism this moment, the sucking disc presses the seat to rotate around the suction pressure inner tube in order to grind the lens.
Preferably, the inner wall of the clutch sleeve 343 is provided with an inner tube seal 345 for being in close contact with the suction-pressure inner tube 341 and a suction seat seal 346 for being in close contact with the suction-pressure seat 342, and a sealed cavity 340 is formed among the clutch sleeve 343, the suction-pressure inner tube 341 and the suction-pressure seat 342. Through at the separation and reunion sleeve inhale and press the inner tube and the sucking disc presses and forms the sealed chamber between the seat, when inhaling the external evacuation equipment of pressure inner tube, the sucking disc presses the seat and can absorb the lens, does not need the manual lens of placing of people, when elevating system drove the lens and descends to the grinding position, separation and reunion drive assembly drive clutch sleeve rises this moment, finishes the evacuation state, can grind.
The side wall of the lower end of the inner pressure absorbing pipe 341 is provided with three branch holes 3412 which are respectively communicated with the inner cavity 3410 and the sealed cavity 340, and the side wall of the upper end of the pressure absorbing seat 342 is provided with three communication holes 3423 which are respectively communicated with the suction holes 3420 and the sealed cavity 340. The utility model provides an inhale and press inside inner tube to be equipped with the inner chamber, carry out the evacuation through the inner chamber, set up 3 forked branches holes and can press 3 suction holes on the seat with the sucking disc to correspond respectively, form vacuum channel, extract air, the atress is even.
Preferably, the clutch driving assembly 344 includes a clutch driving member 3441 disposed on the connecting seat 33 and a linkage assembly 3442 sleeved on the connecting seat 33, wherein one end of the linkage assembly 3442 is connected to the driving end of the clutch driving member 3441, and the other end is connected to the clutch sleeve 343. The linkage includes that 2 covers establish two connecting rods on the connecting seat, carries out the vertical direction through the connecting rod, under the drive effect of separation and reunion driving piece, drives separation and reunion sleeve pipe rebound, and separation and reunion sleeve pipe and sucking disc press the seat, and separation and reunion driving piece is the needle type cylinder in this application embodiment.
Preferably, the swing mechanism 31 includes a swing driving member 311, a transmission assembly and a driving shaft 312; the transmission assembly comprises a driving wheel 313 arranged at the driving end of the swinging driving piece 311, a driven wheel 314 connected with the driving shaft 312, and a synchronous belt 315 respectively sleeved on the driving wheel 313 and the driven wheel 314; the driving shaft 312 is sleeved on the frame 1, and one end of the driving shaft is connected to the driven wheel 314, and the other end is connected to the lifting mechanism 32. The swing driving piece is a stepping motor, and has the advantage that the swing stopping position can be adjusted, so that the full-automatic lens production and processing equipment is reset to the original vertical position, and the lens is conveniently sucked next time.
Preferably, the lifting mechanism 32 includes a fixing plate 321 connected to the driving end of the swing mechanism 31, and a lifting driving member 322 disposed between the fixing plate 321 and the connecting seat 33, wherein the lifting driving member 322 is used for driving the fixing plate 321 to approach or depart from the grinding device 2. Drive lens through elevating system and absorb the group lift, descend to the processing position after absorbing the lens, lift driving piece 52 is the biax cylinder in this application embodiment.
The intelligent feeding and discharging system applied to the full-automatic lens production and processing equipment comprises a feeding and discharging device 5 and a cleaning device 6 which is arranged on one side of the feeding and discharging device 5 and used for cleaning lenses; the feeding and discharging device 5 is used for feeding the lens to be processed and conveying the processed lens to the cleaning device 6 for cleaning, and the feeding and discharging device 5 is also used for discharging the cleaned lens.
The application provides a be applied to unloading system in intelligence of full-automatic lens production and processing equipment, including unloader 5 and belt cleaning device 6, will wait to process the lens material through unloader 5 during the use, the lens rethread unloader 5 that processing was accomplished carries to belt cleaning device 6 and washs, the lens of wasing the completion is at last through unloader 5 unloading on, this application shifts through unloader 5 when the lens adds man-hour, it is automatic to improve, do not need the people to place the lens by hand, avoid polluting the lens.
Preferably, the loading and unloading device 5 includes a loading platform 51, a pick and place mechanism 52 and a conveying mechanism 53. The material loading platform 51 comprises a material loading area for storing lenses to be processed and a material unloading area for storing processed lenses; the taking and placing mechanism 52 is arranged on the upper side of the material loading platform 51, and is used for grabbing the lens to be processed from the material loading area and conveying the lens to be processed to the material loading station 50, and is also used for taking the cleaned lens out of the cleaning device 6 and conveying the lens to the material unloading area for storage; the carrying mechanism 53 is disposed on one side of the pick-and-place mechanism 52, and is configured to grab and convey the lens to be processed from the loading station 50 to the processing station for processing, and convey the processed lens from the processing station to the cleaning device 6 for cleaning. During the use, place the tray of waiting to process the lens and place on the material loading platform, set up the tray that is used for placing the processing and accomplishes the lens simultaneously, snatch on the tray and wait to process the lens and remove to material loading station 50 through getting and putting mechanism 52, rethread transport mechanism 53 will wait to process the lens and snatch and remove and process to the processing equipment in, the lens that the processing was accomplished is snatched and is transferred to belt cleaning device by transport mechanism, wait to wash to accomplish the back again by getting and putting the mechanism and snatch and prevent on the tray the lens that the washing was accomplished, this application improves the automation, need not artifical manual operation, avoid polluting the lens.
Preferably, the pick-and-place mechanism 52 includes a pick-and-place frame 521, a pick-and-place moving group 522, a pick-and-place lifting arm 523, and a pick-and-place sucker 524. The pick-and-place moving group 522 is arranged on the pick-and-place frame 521 and can move on the pick-and-place frame 521 along the horizontal direction; the pick-and-place lifting arm 523 is disposed on the pick-and-place moving group 522 and can lift on the pick-and-place moving group 522 along the vertical direction; and a pick-and-place suction piece 524, which is arranged on the lower side of the pick-and-place lifting arm 523 and is used for sucking lenses. During the use, fix a position the lens through getting and putting removal group 522, remove to waiting to process the lens position, then drop through getting and put the lifing arm and get the piece of gettering to the height with the lens contact, rethread gets and puts the piece of gettering and absorb the lens, get and put the lifing arm and rise the lens and move to material loading station position through getting and putting the removal group, so reciprocal, improve the automation. Preferably, the pick-and-place suction piece 524 is provided with two suction stations, one suction station is used for sucking the lens to the feeding station, and the other suction station is used for taking out the cleaned lens from the cleaning device and moving the lens to the feeding area for storage, so that frequent reciprocation is avoided, and the action path is reduced.
Preferably, the conveying mechanism 53 includes a conveying base 531, a conveying traveling group 532, a conveying lifting arm 533, and a conveying turning arm 53. The conveying moving group 532 is provided on the conveying base 531, and can move on the conveying base 531 in the horizontal direction; a transport lifting arm 533 which is provided on the transport moving group 532 and is capable of vertically lifting on the transport moving group 532; the carrying turning arm 534 is disposed on the carrying lifting arm 533, and is used for sucking the lens. During the use, remove group 532 and remove to material loading station top position through the transport, the transport lift arm descends to the lens position to wait to process lens to the processing station is processed through carrying the upset arm absorption, and processing is accomplished the lens and is taken out again and place on belt cleaning device.
Preferably, the conveying and overturning arm 534 comprises a conveying sliding seat 5341, an overturning bracket 5342 and an overturning driving member 5343. The conveying sliding seat 5341 is slidably disposed on the conveying lifting arm 533; the overturning bracket 5342 is rotatably arranged on the carrying sliding seat 5341, and the end surfaces of the upper side and the lower side of the overturning bracket 5342 are provided with adsorption stations 5340 for absorbing lenses; the turnover driving member 5343 is disposed on the conveying sliding seat 5341 and is used for driving the turnover bracket 5342 to rotate. The purpose that sets up transport upset arm is the effect that can two sides absorption lens, and the lens that processing was accomplished is taken out through the absorption station of one side, and the upset support upset back, the adsorbed lens of another side absorption station will wait to process the lens material loading again, raises the efficiency, avoids too much formation, sets the absorption station to a plurality ofly simultaneously, can serve many processing equipment on same route.
Preferably, the loading station 50 is provided with a pre-positioning device (7) capable of pre-positioning the lens to be processed conveyed by the pick-and-place mechanism 52, and the pre-positioning device (7) comprises a supporting part (71) arranged on the loading station 50 for supporting the lens and a positioning clamping cylinder (72) for pre-clamping the lens on the supporting part (71). The purpose of setting up prepositioning device is with the convenience transport mechanism 53 takes up to carry and ensures the back process precision, avoids positional deviation, shines transport mechanism clamp empty and the problem appears when the material loading.
Preferably, the cleaning device 6 comprises a cleaning bin 61, an opening and closing window group 62, a cleaning clamping mechanism 63 and a spraying mechanism 64. The cleaning bin 61 is provided with a lens inlet 610; the opening and closing window group 62 is arranged on the cleaning bin 61 and used for opening or closing the lens inlet and outlet 610; the cleaning and clamping mechanism 63 is arranged in the cleaning bin 61 and used for clamping or releasing the lens; the spraying mechanism 64 is used for cleaning the lens clamped on the cleaning and clamping mechanism 63. When the lens cleaning machine is used, a processed lens is transferred to the cleaning bin from the lens inlet and outlet through the carrying mechanism, the lens is clamped through the clamping mechanism, the lens inlet and outlet are closed through the opening and closing window set, the lens is cleaned through the spraying mechanism, after the lens is cleaned, the opening and closing window set opens the lens inlet and outlet, and the lens is taken out by the taking and placing mechanism to be subjected to blanking.
Preferably, the spraying mechanism 64 is connected to a gas inlet 641 and a liquid inlet 642, and the spraying mechanism 64 cleans the lens by spraying. This application uses the mode that gas and liquid combine, and the mode of spraying is the aerial fog, can improve the cleaning performance, will grind the residue sanitization of processing back lens.
Preferably, the opening and closing window set 62 includes a switch rotating shaft 621 hinged to the side wall of the cleaning chamber 61, one end of the switch rotating shaft 621 is hinged to an opening and closing window door 622, the other end of the switch rotating shaft 621 is hinged to a switch driving member 623, and the switch driving member 623 drives the switch rotating shaft 621 to rotate relative to the cleaning chamber 61, so that the opening and closing window door 622 opens or closes the lens inlet and outlet 610. Can open or be airtight with the cleaning bin through switch window group, avoid the aerial fog to reveal, influence table surface.
Preferably, the full-automatic lens production and processing equipment comprises a rack 1, and a grinding device 2 and a swinging device 3 which are arranged on the rack 1 at intervals; the grinding device 2 is used for receiving the lens conveyed by the feeding and discharging device 5 and swinging the lens relative to the grinding device 2 to grind.
The above description is only for the purpose of illustrating the preferred embodiments of the present invention and is not to be construed as limiting the invention, and any modifications, equivalents and improvements made within the spirit and principle of the present invention are intended to be included within the scope of the present invention.