Cold stamping die capable of automatically tapping in die
Technical Field
The invention relates to the field of die manufacturing, in particular to a cold stamping die for automatically tapping threads in a die.
Background
The existing cold punching part is assembled through the threaded hole in the cold punching part and the screw fixation, when the cold punching part with the threaded hole is processed, firstly, the cold punching part is formed by punching a punching die and a threaded bottom hole is punched, and then, tapping is carried out outside the die through a tapping machine to produce threads. Because prior art utilizes cold stamping die punching press to go out the screw bottom hole of formed part and formed part earlier, then utilizes the tapping machine to attack the screw thread in the screw bottom hole outside the mould, then need just can accomplish stamping forming and tapping through two frocks, lead to that part processes is many, production efficiency is low, makes manufacturing cost improve, and production cycle is long, is unfavorable for modern technology's high efficiency and quick requirement. In order to overcome the above problems, it is necessary to develop a die integrating punch forming and tapping to overcome the disadvantages of the prior art.
Disclosure of Invention
The invention provides a cold stamping die for automatically tapping threads in a die. The technical scheme is as follows: the method integrates the existing punch forming and tapping, and after the punch forming of a die, tapping of a threaded hole on a stamping part is automatically completed in the die by a tapping machine arranged in the die. The utility model provides an automatic cold stamping die who attacks screw thread in mould, has solved prior art and has gone out the screw thread bottom hole by stamping die stamping forming and punching press earlier, then utilizes to attack tooth machine secondary operation outside the mould and go out the screw thread, and manufacturing procedure is loaded down with trivial details, and production efficiency is low, the problem of production cycle length. The utility model provides an automatic cold stamping die who taps in mould, its beneficial effect is: the thread tapping machine integrates the existing punch forming and thread tapping, and performs thread tapping while punch forming, thereby saving the production cost and shortening the production period.
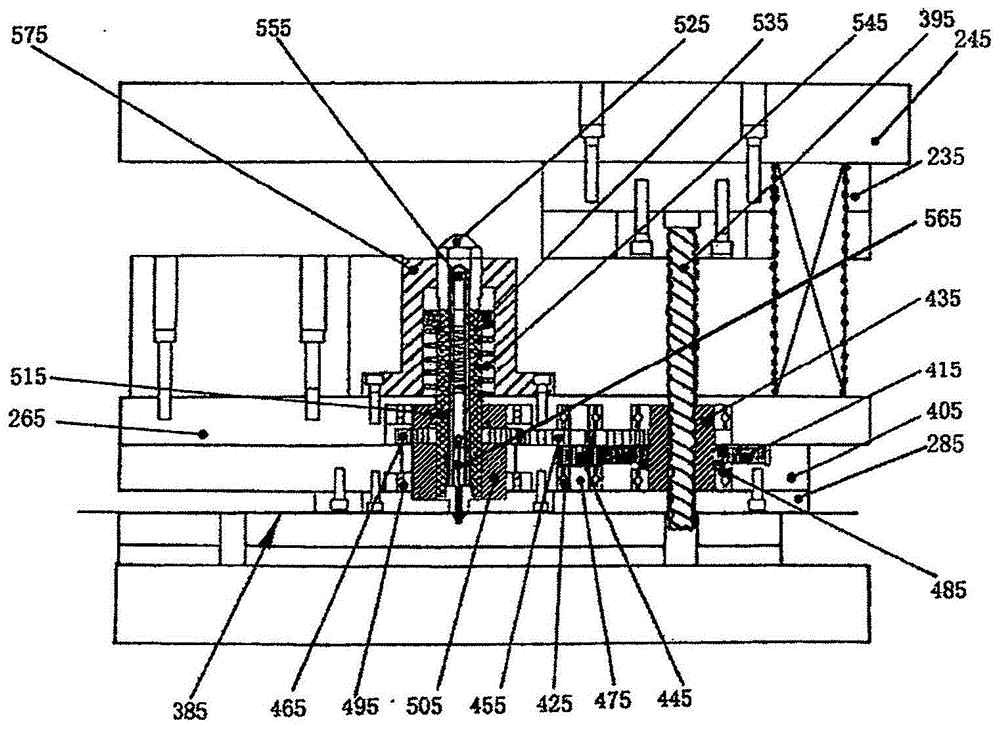
The utility model provides an automatic cold stamping die who taps in mould which characterized by: it includes a punch forming die and an in-die tapping machine 335. The stamping forming die is composed of an upper die and a lower die. (refer to fig. 2 and 1), the upper mold includes: the upper die mounting plate 245 is fixedly connected with the upper die base 235, a first spring mounting hole and a second spring mounting hole are formed in the upper die base 235, a first spring 115 is arranged in the first spring mounting hole, the upper end of the first spring 115 abuts against the lower plane of the upper die mounting plate 245, the lower end of the first spring 115 abuts against the upper end of a limiting screw 125, the discharging plate 175 is in sliding clearance fit with the insert 145, a guide sleeve 165 is fixedly arranged in the discharging plate 175, the guide sleeve 165 is in sliding fit with a guide post 155 arranged in a stepped hole of the upper die mounting plate 205, the discharging backing plate 185 is arranged above the discharging plate 175, the discharging backing plate 185 is tightly attached to the discharging plate 175 under the action of a push rod 195 and a second spring 225, the second spring 225 is arranged in the second spring mounting hole in the upper die base 235, the upper end of the second spring 225 abuts against the lower plane of the upper die mounting plate 245, the lower end of the second spring 225 props against the upper end of the ejector rod 195, the ejector rod 195 is installed in a step hole of the fixing plate 205, the lower end of the ejector rod 195 is tightly attached to the upper plane of the discharging backing plate 185, the discharging plate 175 is fixedly connected with the screw 255, the head of the screw 255 floats up and down in the step hole of the upper die holder 235, when the die is opened, the head of the screw 255 collides with the step of the hole in the upper die holder 235, and the upper die holder 235 is fixedly connected with the fixing backing plate 215 and the fixing plate 205 through the screw. (refer to fig. 4 and 1) the lower mold includes: the die comprises a concave die plate 265, a concave die base plate 275, a lower die base 285, a die foot 295 and a lower die mounting plate 305, wherein the concave die plate 265 is provided with a concave frame, a floating plate 365 is arranged in the provided concave frame, the floating plate 365 is tightly connected with a lower die limiting screw 355, the head of the lower die limiting screw 355 floats in holes of the die foot 295 and the lower die mounting plate 305, a compression spring is sleeved on the lower die limiting screw 355, the upper end of the compression spring props against the lower plane of the floating plate 365, the lower end of the compression spring props against the step of the step hole of the die foot 295, a slider guide 375 is arranged in the step hole of the floating plate 365, the lower end of the slider guide 375 is in sliding fit with the holes in the concave die base plate 275 and the die foot 295, a floating block 325 is arranged above the concave die base plate 275, the floating block 325 is in sliding fit with the holes in the concave die plate 265 and the concave die base plate 275, the, the head of connecting screw 585 is located the downthehole of die leg 295, and the head and the round wire spring contact of connecting screw 585, the lower extreme of round wire spring and the last plane contact of lower mould mounting panel 305, be equipped with float nail 315 in the die board 265, float nail 315 becomes sliding fit with die board 265, and the head of float nail 315 is located the through-hole of die backing plate 275, and the head and the rectangle spring of float nail 315 are hugged closely, and the lower extreme of rectangle spring is hugged closely with the last plane of lower mould mounting panel 305. (please refer to fig. 3 and 5) the in-mold tapping machine 335 includes: the screw die comprises a machine body 405, a screw rod 395, a first gear 415, a first bearing 425, a screw shaft 435, a second gear 445, a third gear 455, a fourth gear 465, a first shaft 475, a second bearing 485, a third bearing 495, a second shaft 505, an elastic shaft sleeve 515, a pressing piece 525, a pressing ring 535, a mounting sleeve 575, a jacket 555 and a screw tap 565, wherein the machine body 405 is fixedly connected with a lower die holder 285, mounting holes of the first bearing 425, the second bearing 485 and the third bearing 495 are arranged in the machine body 405, the first bearing 425, the second bearing 485 and the third bearing 495 are fixedly mounted in the mounting holes arranged in the machine body 405, an inner ring of the second bearing 485 is fixedly sleeved at the lower end of the screw shaft 435, the screw rod 395 rotatably penetrates through the screw hole of the screw shaft 435, the screw rod 395 is fixedly connected with the upper die holder 235 through a screw, the screw shaft 435 is fixedly connected with the screw shaft 435 in a set, the screw shaft 435 is fixedly connected with the, a third gear 455 is arranged above the second gear 445, the third gear 455 is fixedly connected with a first shaft 475 in a set manner, the first shaft 475 is fixedly connected with the second gear 445 in a set manner, the third gear 455 is in meshing and rotating fit with a fourth gear 465, the fourth gear 465 is fixedly connected with a second shaft 505 in a set manner, an inner ring of a third bearing 495 is fixedly connected with the second shaft 505 in a set manner, an elastic shaft sleeve 515 is arranged in the second shaft 505, the elastic shaft sleeve 515 extends into a mounting sleeve 575, the elastic shaft sleeve 515 is sleeved with a spring 545, a pressing ring 535 is arranged above the spring 545, the pressing ring 535 is fixedly connected with the elastic shaft sleeve 515, a clamping sleeve 555 is arranged inside the elastic shaft sleeve 515, the upper end of the clamping sleeve 555 is fixedly connected with a pressing piece 525 in a threaded manner, a screw tap 565 is fixedly connected to the lower end of the clamping sleeve 555, the lower end of the pressing piece is tightly attached to the pressing ring 535, and the lower plane of the pressing ring 535 is tightly attached to the upper, the lower end of the spring 545 is tightly attached to the upper plane of the cavity plate 265, and the installation sleeve 575 is tightly connected with the cavity plate 265 through screws.
Drawings
The invention will be further explained with reference to the drawings
Shown in the figure:
fig. 1 is a schematic view of the assembly of the upper die, lower die and in-die tapping machine 335.
Fig. 2 is a schematic structural view of the upper mold in the direction b in fig. 1.
Fig. 3 is a schematic view of the connection between the b-direction in-mold tapping machine 335 and the mold in fig. 1.
Fig. 4 is a partial schematic view of the longitudinal in-mold tapping machine 335 of fig. 1 coupled to a mold.
Fig. 5 is a schematic view of the connection between the rotating mechanism and the mold of the in-mold tapping machine 335.
115-first spring 125-limit screw 145-insert
155-guide post 165-guide sleeve 175-stripper plate
185-unloading backing plate 195-top rod 205-fixing plate
215-fixed backing plate 225-second spring 235-upper die base
245-upper die mounting plate 255-screw 265-concave die plate
275 die backing plate 285 die base 295 die leg
305-lower die mounting plate 315-floating nail 325-floating block
335-in-mold tapping machine 355-lower limit screw 365-floating plate
375-guide slide piece 385-strip 395-screw rod
405-body 425-first bearing 435-screw shaft
445-second gear 455-third gear 465-fourth gear
475-first shaft 485-second bearing 495-third bearing
505-second shaft 515-elastic shaft sleeve 525-pressing piece
535-pressing ring 545-spring 555-jacket
565-screw tap 575-mounting sleeve 585-connecting screw
The specific implementation mode is as follows:
the cold stamping die with the automatic tapping in the die is shown in the figure, and the working principle and the structural connection of the cold stamping die are explained in detail below.
Firstly, constructing and connecting: a cold stamping die capable of tapping threads automatically in a die comprises a stamping forming die and a die inner tapping machine 335. The stamping forming die is composed of an upper die and a lower die. (refer to fig. 2 and 1), the upper mold includes: the upper die mounting plate 245 is fixedly connected with the upper die base 235, a first spring mounting hole and a second spring mounting hole are formed in the upper die base 235, a first spring 115 is arranged in the first spring mounting hole, the upper end of the first spring 115 abuts against the lower plane of the upper die mounting plate 245, the lower end of the first spring 115 abuts against the upper end of a limiting screw 125, the discharging plate 175 is in sliding clearance fit with the insert 145, a guide sleeve 165 is fixedly arranged in the discharging plate 175, the guide sleeve 165 is in sliding fit with a guide post 155 arranged in a stepped hole of the upper die mounting plate 205, the discharging backing plate 185 is arranged above the discharging plate 175, the discharging backing plate 185 is tightly attached to the discharging plate 175 under the action of a push rod 195 and a second spring 225, the second spring 225 is arranged in the second spring mounting hole in the upper die base 235, the upper end of the second spring 225 abuts against the lower plane of the upper die mounting plate 245, the lower end of the second spring 225 props against the upper end of the ejector rod 195, the ejector rod 195 is installed in a step hole of the fixing plate 205, the lower end of the ejector rod 195 is tightly attached to the upper plane of the discharging backing plate 185, the discharging plate 175 is fixedly connected with the screw 255, the head of the screw 255 floats up and down in the step hole of the upper die holder 235, when the die is opened, the head of the screw 255 collides with the step of the hole in the upper die holder 235, and the upper die holder 235 is fixedly connected with the fixing backing plate 215 and the fixing plate 205 through the screw. (refer to fig. 4 and 1) the lower mold includes: the die comprises a concave die plate 265, a concave die base plate 275, a lower die base 285, a die foot 295 and a lower die mounting plate 305, wherein the concave die plate 265 is provided with a concave frame, a floating plate 365 is arranged in the provided concave frame, the floating plate 365 is tightly connected with a lower die limiting screw 355, the head of the lower die limiting screw 355 floats in holes of the die foot 295 and the lower die mounting plate 305, a compression spring is sleeved on the lower die limiting screw 355, the upper end of the compression spring props against the lower plane of the floating plate 365, the lower end of the compression spring props against the step of the step hole of the die foot 295, a slider guide 375 is arranged in the step hole of the floating plate 365, the lower end of the slider guide 375 is in sliding fit with the holes in the concave die base plate 275 and the die foot 295, a floating block 325 is arranged above the concave die base plate 275, the floating block 325 is in sliding fit with the holes in the concave die plate 265 and the concave die base plate 275, the, the head of connecting screw 585 is located the downthehole of die leg 295, and the head and the round wire spring contact of connecting screw 585, the lower extreme of round wire spring and the last plane contact of lower mould mounting panel 305, be equipped with float nail 315 in the die board 265, float nail 315 becomes sliding fit with die board 265, and the head of float nail 315 is located the through-hole of die backing plate 275, and the head and the rectangle spring of float nail 315 are hugged closely, and the lower extreme of rectangle spring is hugged closely with the last plane of lower mould mounting panel 305. (please refer to fig. 3 and 5) the in-mold tapping machine 335 includes: the screw die comprises a machine body 405, a screw rod 395, a first gear 415, a first bearing 425, a screw shaft 435, a second gear 445, a third gear 455, a fourth gear 465, a first shaft 475, a second bearing 485, a third bearing 495, a second shaft 505, an elastic shaft sleeve 515, a pressing piece 525, a pressing ring 535, a mounting sleeve 575, a jacket 555 and a screw tap 565, wherein the machine body 405 is fixedly connected with a lower die holder 285, mounting holes of the first bearing 425, the second bearing 485 and the third bearing 495 are arranged in the machine body 405, the first bearing 425, the second bearing 485 and the third bearing 495 are fixedly mounted in the mounting holes arranged in the machine body 405, an inner ring of the second bearing 485 is fixedly sleeved at the lower end of the screw shaft 435, the screw rod 395 rotatably penetrates through the screw hole of the screw shaft 435, the screw rod 395 is fixedly connected with an upper die holder 235 through a screw, the screw shaft 435 is fixedly connected with the screw shaft 435, the screw shaft 435 in a set fixedly connected with the first gear 415, a third gear 455 is arranged above the second gear 445, the third gear 455 is fixedly connected with a first shaft 475 in a set manner, the first shaft 475 is fixedly connected with the second gear 445 in a set manner, the third gear 455 is in meshing and rotating fit with a fourth gear 465, the fourth gear 465 is fixedly connected with a second shaft 505 in a set manner, an inner ring of a third bearing 495 is fixedly connected with the second shaft 505 in a set manner, an elastic shaft sleeve 515 is arranged in the second shaft 505, the elastic shaft sleeve 515 extends into a mounting sleeve 575, the elastic shaft sleeve 515 is sleeved with a spring 545, a pressing ring 535 is arranged above the spring 545, the pressing ring 535 is fixedly connected with the elastic shaft sleeve 515, a clamping sleeve 555 is arranged inside the elastic shaft sleeve 515, the upper end of the clamping sleeve 555 is fixedly connected with a pressing piece 525 in a threaded manner, a screw tap 565 is fixedly connected to the lower end of the clamping sleeve 555, the lower end of the pressing piece is tightly attached to the pressing ring 535, and the lower plane of the pressing ring 535 is tightly attached to the upper, the lower end of the spring 545 is tightly attached to the upper plane of the cavity plate 265, and the installation sleeve 575 is tightly connected with the cavity plate 265 through screws.
II, the working principle is as follows: (refer to fig. 3 and 5) when the die is mounted on the punching machine, during punching, firstly, the punching die punches the former forming stations, as the length of material forming the threaded hole is fed into the step, the length of material forming the threaded hole is below the tap 565, while the upper die is lowered, during this action, the screw shaft 395 rotates the screw shaft 435, so that the first gear 415 fixedly connected to the screw shaft 435 rotates the second gear 445, the second gear 445 rotates the first shaft 475, so that the third gear 455 fixedly connected to the first shaft 475 rotates the fourth gear 465, because the fourth gear 465 is tightly matched with the elastic shaft sleeve 515, the elastic shaft sleeve 515 is tightly attached to the jacket 555, so that the fourth gear 465 drives the screw tap 565 clamped in the jacket 555 to rotate clockwise, while the upper die descends, the in-die tapping machine 335 causes the tap 565 to tap the section of material that is fed below. During tapping, as the jacket 555 and the elastic shaft sleeve 515 are matched together in a T-shaped sliding manner, the elastic shaft sleeve 515 is supported by the spring 545, so that the head of the tap 565 of the elastic shaft sleeve 515 is retracted in the floating plate 365, when the upper die descends, the screw shaft 395 and the first gear 415 are driven by the screw shaft 395 to rotate, the first gear 415 drives the second gear 445, the first shaft 475 and the third gear 455 to rotate, the third gear 455 drives the fourth gear 465 and the second shaft 505 to rotate, as the second shaft 505 is tightly matched and connected with the elastic shaft sleeve 515, the elastic shaft sleeve 515 is tightly clung to the jacket 555, so that the tap 565 clamped in the jacket 555 rotates along with the jacket 555, the upper die descends continuously, when the lower plane of the upper die holder 235 is contacted with the pressing piece 525, the upper die holder 235 forces the pressing piece 525 to drive the jacket 555 to slide down along the T-shaped groove on the inner side wall of the elastic shaft sleeve 515, so that the tap 565 connected to, at this time, the tap 565 rotates downward to tap the thread. When the upper die ascends after the tapping is finished, the screw rod 395 drives the first gear 415, the second gear 445, the third gear 455 and the fourth gear 465 to reversely rotate when the upper die descends, and then the screw tap 565 reversely rotates to exit from the tapped threaded hole. [ note: when the upper die moves upward, the upper die base 235 is separated from the pressing member 525, and the spring 545 loses pressure, and the tap 565 is withdrawn from the threaded hole by the upward movement of the spring 545 while rotating in the reverse direction. The upper die continues to travel upward and the tap 565 retracts into the float plate 365.