Disclosure of Invention
The invention aims to provide a waste heat recovery system, which is used for solving the technical problems of low recovery utilization rate of tail gas heat energy and high cost of the waste heat recovery system of the existing gas-fired boiler; the invention also aims to provide a waste heat recovery method and a boiler system which can solve the technical problems of low waste heat recovery rate and high waste heat recovery cost of the tail gas of the gas-fired boiler.
The technical scheme of the waste heat recovery system is as follows:
a waste heat recovery system comprising:
the first heat exchanger is arranged in the flue, is an air-water heat exchanger and is internally provided with a first internal pipeline; the first heat exchanger can realize the first recovery of heat in the tail gas (flue gas), and the temperature of the first heat exchange medium can be increased while the heat is recovered, so that the temperature of the first heat exchange medium is higher than the condensation temperature of water vapor in the tail gas, and the water vapor in the tail gas is prevented from condensing on the outer surface of the first heat exchanger, thereby playing an important role in preventive corrosion prevention and essentially performing a corrosion prevention function;
the second heat exchanger is arranged in the flue and is positioned behind the first heat exchanger, the second heat exchanger is an air-water heat exchanger and is provided with a second internal pipeline, and the second internal pipeline is provided with a cooling water inlet and a cooling water outlet; the second heat exchanger can realize the second recovery of heat in the tail gas, and because a second heat exchange medium (cooling water) is introduced into the second heat exchanger and is lower than the condensation temperature of water vapor in the tail gas, the water vapor in the tail gas can be greatly condensed on the outer surface of the second heat exchanger, and the condensation is a violent phase change process, so that a large amount of heat can be generated, and the second heat exchanger can also quickly and efficiently collect the heat in the tail gas;
the third heat exchanger is a plate heat exchanger for water-water heat exchange, a hot end pipeline and a cold end pipeline which are mutually crossed and attached are arranged in the third heat exchanger, an inlet of the cold end pipeline is communicated with the cooling water outlet, and an outlet of the cold end pipeline is communicated with a water inlet pipeline of the gas-fired boiler; the third heat exchanger can recover heat in the first heat exchange medium, so that the heat in the first heat exchange medium can be transferred to a second heat exchange medium serving as an output medium, the heat is indirectly recovered for the third time, and the heat in the tail gas can be output to the second heat exchange medium as much as possible for subsequent use; on the other hand, the third heat exchanger is also a control mode for the temperature of the first heat exchange medium while realizing the heat exchange between the first heat exchange medium and the second heat exchange medium, so that the first heat exchange medium is maintained within a range slightly higher than the dew point temperature, and the heat exchange efficiency of the first heat exchanger is improved as much as possible on the premise of corrosion resistance; moreover, the third heat exchanger is a plate heat exchanger, the contact area between the two heat exchange media of the plate heat exchanger is larger, and the contact time is longer, so that the plate heat exchanger can better and more efficiently realize the heat exchange efficiency of the first heat exchange medium and the second heat exchange medium;
the first internal pipeline and the hot end pipeline are communicated through a water pipe to form an internal circulation pipeline, the internal circulation pipeline further comprises a driving module, a first heat exchange medium which circularly flows under the driving of the driving module is filled in the internal circulation pipeline, and a temperature detection module for monitoring the temperature of the first heat exchange medium in the first internal pipeline is further arranged on the internal circulation pipeline; the temperature of the first heat exchange medium can be conveniently controlled by the arrangement of the internal circulation pipeline, and the effective operation of the first heat exchanger and the third heat exchanger is realized, the structural design is very ingenious, and the heat regeneration efficiency is realized without increasing too much cost;
the controller is in control connection with the temperature detection module and the driving module, controls the driving module according to the feedback of the temperature detection module, and controls the temperature of the first heat exchange medium to be within a set temperature range in a mode of adjusting the flow of the first heat exchange medium; the controller, the driving module and the temperature detection module are arranged to automatically control the temperature, so that the first heat exchange medium is ensured to be in a high-efficiency heat exchange state all the time, and the heat recovery efficiency is improved;
and the second heat exchange medium enters the second internal pipeline from the cooling water inlet to perform primary heat exchange with the flue gas, and flows to the cold end pipeline of the third heat exchanger from the cooling water outlet so as to perform secondary heat exchange with the first heat exchange medium flowing in the hot end pipeline. The second heat exchange medium is used as a working medium or an output medium and is used for absorbing heat in the tail gas and conveying the heat out for secondary utilization; the second heat exchange medium is introduced into the water inlet pipeline of the steam boiler, so that the temperature of the starting point of the gas boiler is increased when the gas boiler is used for heating and producing steam, the heat consumed by the steam production is obviously reduced, and the utilization rate of energy is increased.
On the basis of the scheme, the cross section of the first inner pipeline of the first heat exchanger is oval, and the length direction of the oval is arranged along the flow direction of the flue gas.
On the basis of the scheme, the heat exchanger is further improved as follows, and the first heat exchanger is a finned tube heat exchanger.
On the basis of the scheme, the driving module is a circulating water pump arranged on the inner circulating pipeline. The arrangement of the circulating water pump can facilitate the controller to control the rotating speed of the circulating water pump in a mode of controlling the frequency of the circulating water pump.
The technical scheme of the waste heat recovery method is as follows:
a method of waste heat recovery comprising the steps of:
s10, sequentially arranging a first heat exchanger and a second heat exchanger for air-water heat exchange in the flue along the flow direction of flue gas, wherein the first heat exchanger and the second heat exchanger are respectively provided with a first internal pipeline and a second internal pipeline;
s20, arranging a third heat exchanger outside the range of the smoke cover, wherein the third heat exchanger is a water-water heat exchanger with a hot end pipeline and a cold end pipeline;
s30, communicating the first internal pipeline with the hot end pipeline to form an internal circulation pipeline, arranging a temperature detection module on the first internal pipeline, filling a first heat exchange medium into the internal circulation pipeline, and arranging a driving module to drive the first heat exchange medium to flow;
s40, connecting a cooling water outlet of the second internal pipeline with an inlet of the cold end pipeline through a water pipe, connecting a cooling water inlet of the second internal pipeline with a cooling water supply system, connecting an outlet of the cold end pipeline with a water inlet pipeline of the gas-fired boiler through a water pipe, and introducing a second heat exchange medium through the cooling water inlet;
s50, setting a controller to be in control connection with the driving module and the temperature detection module, setting a temperature range through the controller, enabling the set lowest temperature to be higher than the dew point temperature of vapor in the flue gas when the vapor is condensed on the outer surface of the first heat exchanger, setting the highest temperature to be infinitely close to the lowest temperature so as to improve the heat exchange efficiency, comparing the temperature of the first heat exchange medium detected by the temperature detection module with the set temperature range, controlling the driving module to operate slowly to reduce the flow of the first heat exchange medium when the detected actual temperature is lower than the set lowest temperature, and controlling the driving module to operate quickly to improve the flow of the first heat exchange medium when the detected actual temperature is higher than the set highest temperature.
On the basis of the scheme, the first heat exchanger is further improved in the following mode, the first inner pipeline with the oval cross section is selected for the first heat exchanger, and the oval length direction is arranged along the flow direction of the flue gas.
On the basis of the scheme, the heat exchanger is further improved as follows, and the first heat exchanger is a finned tube heat exchanger.
On the basis of the above scheme, the driving module further comprises a circulating water pump, and the circulating water pump is arranged on the internal circulating pipeline in S30.
The technical scheme of the boiler system is as follows:
boiler system, including boiler body, the flue and the inlet tube that link to each other with boiler body, still include:
the first heat exchanger is arranged in the flue, is an air-water heat exchanger and is internally provided with a first internal pipeline; the first heat exchanger can realize the first recovery of heat in the tail gas (flue gas), and the temperature of the first heat exchange medium can be increased while the heat is recovered, so that the temperature of the first heat exchange medium is higher than the condensation temperature of water vapor in the tail gas, the water vapor in the tail gas is prevented from condensing on the outer surface of the first heat exchanger, and an important essential anticorrosion effect is achieved;
the second heat exchanger is arranged in the flue and is positioned behind the first heat exchanger, the second heat exchanger is an air-water heat exchanger and is provided with a second internal pipeline, and the second internal pipeline is provided with a cooling water inlet and a cooling water outlet; the second heat exchanger can realize the second recovery of heat in the tail gas, and because a second heat exchange medium (cooling water) is introduced into the second heat exchanger and is lower than the condensation temperature of water vapor in the tail gas, the water vapor in the tail gas can be greatly condensed on the outer surface of the second heat exchanger, and the condensation is a violent phase change process, so that a large amount of heat can be generated, and the second heat exchanger can also quickly and efficiently collect the heat in the tail gas;
the third heat exchanger is a plate heat exchanger for water-water heat exchange, a hot end pipeline and a cold end pipeline which are mutually crossed and attached are arranged in the third heat exchanger, an inlet of the cold end pipeline is communicated with the cooling water outlet, and an outlet of the cold end pipeline is communicated with a water inlet pipeline of the gas-fired boiler; the third heat exchanger can recover heat in the first heat exchange medium, so that the heat in the first heat exchange medium can be transferred to a second heat exchange medium serving as an output medium, the heat is indirectly recovered for the third time, and the heat in the tail gas can be output to the second heat exchange medium as much as possible for subsequent use; on the other hand, the third heat exchanger is also a control mode for the temperature of the first heat exchange medium while realizing the heat exchange between the first heat exchange medium and the second heat exchange medium, so that the first heat exchange medium is maintained within a range slightly higher than the dew point temperature, and the heat exchange efficiency of the first heat exchanger is improved as much as possible on the premise of corrosion resistance; moreover, the third heat exchanger is a plate heat exchanger, the contact area between the two heat exchange media of the plate heat exchanger is larger, and the contact time is longer, so that the plate heat exchanger can better and more efficiently realize the heat exchange efficiency of the first heat exchange medium and the second heat exchange medium;
the first internal pipeline and the hot end pipeline are communicated through a water pipe to form an internal circulation pipeline, the internal circulation pipeline further comprises a driving module, a first heat exchange medium which circularly flows under the driving of the driving module is filled in the internal circulation pipeline, and a temperature detection module for monitoring the temperature of the first heat exchange medium in the first internal pipeline is further arranged on the internal circulation pipeline; the temperature of the first heat exchange medium can be conveniently controlled by the arrangement of the internal circulation pipeline, and the effective operation of the first heat exchanger and the third heat exchanger is realized, the structural design is very ingenious, and the heat regeneration efficiency is realized without increasing too much cost;
the controller is in control connection with the temperature detection module and the driving module, controls the driving module according to the feedback of the temperature detection module, and controls the temperature of the first heat exchange medium to be within a set temperature range in a mode of adjusting the flow of the first heat exchange medium; the controller, the driving module and the temperature detection module are arranged to automatically control the temperature, so that the first heat exchange medium is ensured to be in a high-efficiency heat exchange state all the time, and the heat recovery efficiency is improved;
and the second heat exchange medium enters the second internal pipeline from the cooling water inlet to perform primary heat exchange with the flue gas, and flows to the cold end pipeline of the third heat exchanger from the cooling water outlet so as to perform secondary heat exchange with the first heat exchange medium flowing in the hot end pipeline. The second heat exchange medium is used as a working medium or an output medium and is used for absorbing heat in the tail gas and conveying the heat out for secondary utilization; the second heat exchange medium is introduced into the water inlet pipeline of the steam boiler, so that the temperature of the starting point of the gas boiler is increased when the gas boiler is used for heating and producing steam, the heat consumed by the steam production is obviously reduced, and the utilization rate of energy is increased.
On the basis of the scheme, the cross section of the first inner pipeline of the first heat exchanger is oval, and the length direction of the oval is arranged along the flow direction of the flue gas.
On the basis of the scheme, the heat exchanger is further improved as follows, and the first heat exchanger is a finned tube heat exchanger.
The invention has the beneficial effects that: the invention has high heat recovery efficiency and can improve the energy utilization rate as much as possible, firstly, the temperature of the first heat exchange medium in the first heat exchanger is controlled to be as low as possible on the premise that the temperature is higher than the dew point and is not easy to corrode, thus the heat exchange efficiency is higher when the first heat exchange is carried out with tail gas; secondly, the first heat exchanger adopts finned tubes with oval cross sections, and the heat exchange efficiency is further improved because the width of the finned tubes in the wind direction is wider on the premise of meeting the requirement of smaller wind resistance, and therefore, the heat exchange time is longer, the heat exchange area is larger; in addition, the first heat exchanger does not condense, so that the heat exchanger with fins is selected, the heat exchange efficiency of the fins is high, and the heat recovery efficiency is improved; moreover, the first heat exchange medium realizes heat exchange with the second heat exchange medium through the third heat exchanger, so that the temperature of the second heat exchange medium serving as an output product is further increased, and the heat recovery efficiency is further improved; more importantly, the heated first heat exchange medium is used as raw material water of the gas boiler, so that the fuel quantity required by the gas boiler when heating the first heat exchange medium is obviously reduced compared with the fuel quantity required by the original cooling water used as the raw material, namely, the energy dissipation during subsequent long-distance conveying is avoided, and the starting point temperature of the gas boiler during steam production is increased, so that the energy utilization rate is improved; therefore, the waste heat recovery system and the waste heat recovery method have high heat recovery efficiency, and can improve the energy utilization rate of the gas-fired boiler as much as possible.
Detailed Description
In order to make the objects, technical solutions and advantages of the present invention more apparent, the present invention is described in further detail below with reference to the accompanying drawings and embodiments. It should be understood that the detailed description and specific examples, while indicating the preferred embodiment of the invention, are intended for purposes of illustration only and are not intended to limit the scope of the invention. The components of embodiments of the present invention generally described and illustrated in the figures herein may be arranged and designed in a wide variety of different configurations.
Thus, the following detailed description of the embodiments of the present invention, presented in the figures, is not intended to limit the scope of the invention, as claimed, but is merely representative of selected embodiments of the invention. All other embodiments, which can be derived by a person skilled in the art from the embodiments of the present invention without making any creative effort, shall fall within the protection scope of the present invention.
It is noted that relational terms such as "first" and "second," and the like, may be used solely to distinguish one entity or action from another entity or action without necessarily requiring or implying any actual such relationship or order between such entities or actions. Also, the terms "comprises," "comprising," or any other variation thereof, are intended to cover a non-exclusive inclusion, such that a process, method, article, or apparatus that comprises a list of elements does not include only those elements but may include other elements not expressly listed or inherent to such process, method, article, or apparatus. Without further limitation, an element defined by the phrase "comprising an … …" does not exclude the presence of other identical elements in a process, method, article, or apparatus that comprises the element.
The features and properties of the present invention are described in further detail below with reference to examples.
Embodiment 1 of the waste heat recovery system of the present invention:
the waste heat recovery system is used for waste heat recovery of tail gas of a gas boiler or a coal-fired boiler, and is provided with a shell 40, wherein the shell 40 is in a pipeline shape and is connected in a tail gas pipeline in series, namely, two ends of the shell are in sealed butt joint with a tail gas pipe respectively, so that the tail gas of the boiler can pass through the waste heat recovery system, the tail gas is discharged after heat exchange is carried out, heat in the tail gas is transferred to a heat transfer medium of the waste heat recovery system, heating is carried out by utilizing the heat of the heat transfer medium, and the like. More specifically:
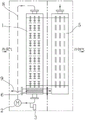
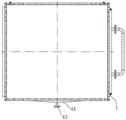
as shown in fig. 1 to 4, the waste heat recovery system includes a housing 40 and a first heat exchanger 1, a second heat exchanger 5, and a third heat exchanger 6 installed in the housing 40. Wherein:
the first heat exchanger 1 is a tube fin type air-water heat exchanger made of common carbon steel, tube fins of the first heat exchanger are elliptical finned tubes, the windward side of the first heat exchanger is small, the heat exchange area is large, the wind resistance outside the tubes can be fully reduced on the premise of ensuring the heat exchange efficiency, the overall structure better conforms to the field synergy principle, and the heat transfer coefficient of the first heat exchanger is superior to that of a common circular finned tube. Meanwhile, in order to ensure the corrosion resistance of the heat exchanger in the area, the outside of the finned tube is galvanized. Through high-temperature hot galvanizing, the fins and the base pipe are wrapped by the zinc layer at the same time, and the protection of the zinc layer can ensure that the fin and the base pipe have antirust and anticorrosive performances while the high-efficiency heat transfer between metals is kept. The following table is a table of performance parameters of the elliptical finned tube heat exchanger (first heat exchanger 1):
the body of first heat exchanger 1 is last to have circulating water import 11 and circulating water export 12, and what match with first heat exchanger 1 has an inner loop pipeline, and the inner loop pipeline includes circulating water pump 2, level pressure jar 3, converter and pipeline etc. and wherein the setting of level pressure jar 3 is for stabilizing water pressure. The pipeline is connected with a circulating water inlet 11 and a circulating water outlet 12 of the first heat exchanger 1 to form a closed-loop internal circulation pipeline, a circulating water pump 2, a constant pressure tank 3 and the like are arranged on the internal circulation pipeline, under the control of a frequency converter, the circulating water pump 2 operates according to a set rotating speed, so that a heat exchange medium (generally water, referred to as a first heat exchange medium 8) in the internal circulation pipeline circularly flows according to a set flow (flow speed), and exchanges heat with high-temperature flue gas (generally around 110-. Meanwhile, the internal circulation pipeline is also connected with the third heat exchanger 6, performs heat exchange with another heat exchange medium (cooling water heated by the second heat exchanger 5, referred to as a second heat exchange medium 9) in the third heat exchanger 6, transfers the heat to the second heat exchange medium 9, and realizes temperature control of the first heat exchange medium 8; through the control of converter and circulating water pump 2 to 8 velocity of flow (flows) of first heat transfer medium and with the heat exchange of second heat transfer medium 9 promptly, realized the control to 8 temperatures of first heat transfer medium for 8 temperatures of first heat transfer medium are a little higher than dew point temperature (the condensation temperature of the vapor in the tail gas on 1 outer pipe wall of first heat exchanger), when guaranteeing that tail gas can not condense in vapor, 8 temperatures of first heat transfer medium are as low as possible, thereby improve 1 heat exchange efficiency of first heat exchanger.
In order to facilitate the control of the water temperature in the internal circulation pipeline, a temperature detection sensor is arranged on the internal circulation pipeline, a temperature range which can ensure that the water vapor in the tail gas is condensed and can also ensure that the heat exchange efficiency is higher is set, for example, 65-75 c is set as the temperature range, when the temperature sensor detects that the actual temperature is lower than 65 c, it is necessary to control the rotation speed of the circulating water pump 2, the flow is slower, so that the heat exchange time of the first heat exchange medium 8 and the high-temperature tail gas is prolonged, thereby increasing the temperature of the first heat exchange medium 8, whereas if the actual temperature is detected to be higher than 75 c, the rotating speed of the circulating water pump 2 needs to be controlled, so that the flow speed is fast, the heat exchange time of the first heat exchange medium 8 and the high-temperature tail gas is shortened, and the purpose of controlling the water temperature of the first heat exchange medium 8 within a set range is achieved.
It should be noted that: the reason why the water vapor in the exhaust gas is prevented from condensing on the outer surface of the first heat exchanger 1 is that the exhaust gas contains a large amount of nitrogen oxides and water vapor after the natural gas is sufficiently combusted. When the tail gas passes through the first heat exchanger 1, if the temperature of the first heat exchange medium 8 in the first heat exchanger 1 is lower than the dew point temperature, water vapor in the tail gas is separated out due to condensation and is combined with nitrogen oxides to generate a nitric acid solution. Due to the structural action of the fins, the acidic corrosive solution collects liquid drops outside the fin tubes of the heat exchanger, so that the fins are gradually corroded to generate metal oxides (rust). The fluffy oxides are accumulated outside the first heat exchanger 1, so that an air channel is gradually blocked, the air outlet resistance in the pipeline is increased, the performance working point of the tail gas fan is changed, and the air volume is obviously reduced. In the scheme of the invention, the temperature of the first heat exchange medium 8 is controlled to be slightly higher than the dew point through the arrangement of the internal circulation pipeline and the third heat exchanger 6, so that the acidic corrosive solution cannot be condensed on the outer surface of the first heat exchanger 1, and the corrosion problem of the first heat exchanger 1 is avoided.
High anticorrosive material, for example stainless steel or the heat exchange tube of taking special cladding can effectively be able to bear the corrosion of rare nitric acid, but because its price is more expensive, if all use high anticorrosive material to make the heat exchanger, probably lead to the heat exchanger investment cost far beyond the budget. Considering the cost, first heat exchanger 1 itself can choose ordinary carbon steel material not corrosion-resistant for use, owing to avoided first heat exchanger 1 surface corrosion through 8 temperature's of first heat transfer medium control, does not worry again under the prerequisite of anticorrosive problem, chooses for use the heat exchanger that the cross section is oval fin tube structure for the purpose of improving heat exchange efficiency. In other words, the temperature of the entire flow field of the exhaust gas as it passes through the condenser is calculated according to software simulation. And in different temperature intervals, different materials are selected for use as the heat exchange tube material, so that the heat exchanger structure with the heat exchange tube material coupled with the temperature field is realized. In the high-temperature area of the condenser, because no water is analyzed, the finned tube made of common materials can be combined with common anticorrosion measures to inhibit acid corrosion. In the low temperature region, a large amount of dilute nitric acid solution is formed because a large amount of water is separated out. Therefore, in this region, stainless steel light pipes, which are corrosion resistant but costly, are selected for the design of the condenser module in which the region is fabricated (see below for further details).
The high-temperature flue gas further enters a second heat exchanger 5 after passing through the first heat exchanger 1. As shown in fig. 3, the second heat exchanger 5 is a light-pipe air-water heat exchanger made of stainless steel, and a body of the heat exchanger is provided with a cooling water inlet 51 and a cooling water outlet 52 for the second heat exchange medium 9 to flow through, and the second heat exchange medium 9 is mainly used for heating the second heat exchange medium 9 to a required temperature, and the second heat exchange medium 9 is an output product of the waste heat recovery system, and can be used for heating or a water supply system of a gas boiler, so that the gas boiler can consume a little fuel when producing steam. In the second heat exchanger 5, as the temperature of the second heat exchange medium 9 in the second heat exchanger is lower than the dew point temperature, a large amount of heat is released by condensation of water vapor in the flue gas, and the heating power during the whole condensation can account for about 11% of the full heat value of the natural gas at most. In order to ensure reliable construction, a certain margin is reserved, and the flue gas temperature is recovered to 50 ℃. In the second heat exchanger 5, since the flue gas is mainly saturated steam, a large amount of heat is released along with condensation, and a large amount of condensed water is separated out. At this time, a large amount of acidic solution is generated outside the heat exchange tube.
The second-stage heat exchanger is a condensation heat exchange core area, and because the phase change of condensation heat exchange is severe and the heat exchange amount is large, the heat exchange efficiency is not required to be increased by adopting fins, and the light tube made of stainless steel or glass is directly adopted in consideration of the requirements on cost and corrosion resistance. The following table is a table of performance parameters for the bare tube heat exchanger (second heat exchanger 5):
as shown in fig. 3 and 4, since the acid solution is formed on the surface of the second heat exchanger 5, the acid solution is unfavorable to the heat exchanger on the surface of the heat exchanger, and dust is easily accumulated, a spray pipe 4 is disposed between the first heat exchanger 1 and the second heat exchanger 5, a plurality of spray nozzles 41 are disposed at intervals on the spray pipe 4, the spray nozzles 41 are disposed toward the second heat exchanger 5, high-pressure water is supplied by an external water supply pump, supplied to the spray pipe 4 through a spray water inlet 42, high-pressure water mist is sprayed out through the spray nozzles 41 in a tapered range to wash off the outer surface of the second heat exchanger 5 on-line, so as to wash off the dust and the acid solution on the surface of the second heat exchanger 5, a water collection tank 44 structure similar to a funnel is disposed at the lower portion of the housing 40 corresponding to the second heat exchanger 5, a water discharge port 43 is disposed at the lower portion of the water collection tank structure for discharging the washed off, it is therefore contemplated that the acidic solution may be filtered, purified, etc. to form a more pure acidic solution for subsequent use. In other embodiments, the material of the light pipe may be replaced by a corrosion-resistant material such as glass or ceramic.
Meanwhile, due to the separation of the condensed water, dust and impurities are very easily polluted in the area, so that the drawer type core body is adopted in the design, the maintenance and the cleaning are convenient, and the efficiency of the heat exchange tube and the cleanliness in the area are improved.
The third heat exchanger 6 is an auxiliary heat exchanger for exchanging heat between the internal heat exchange media (the first heat exchange medium 8 and the second heat exchange medium 9) of the first heat exchanger 1 and the second heat exchanger 5, the plate heat exchanger adopts a plate heat exchanger with a multi-layer plate stack structure, is a water-water heat exchanger, does not participate in heat exchange with tail gas, and has the main function of matching with an internal circulation pipeline system to conveniently control the temperature of the first heat exchange medium 8, and secondly, can perform secondary heating on the second heat exchange medium 9 to further improve the temperature of the second heat exchange medium 9.
In other words, the first heat exchanger 1 and the third heat exchanger 6 can be regarded as one first-stage heat exchanger, the second heat exchanger 5 is a second-stage heat exchanger, the first-stage heat exchanger is provided with internal circulation medium temperature control (namely provided with a plate heat exchanger, namely the third heat exchanger 6), namely, three streams of fluid exist in the first-stage heat exchanger, and the heat medium (the first heat exchange medium 8), the cold medium (the second heat exchange medium 9) and the high-temperature flue gas form two heat transfer states among the three. As shown in fig. 1, the three heat exchangers are integrated into a single structure. In order to meet the on-site transportation limit of the equipment and consider the convenience of equipment transportation and installation, the equipment is split into at least two templates.
On the other hand, the system is also provided with a water leakage alarm module and a water shortage alarm module, and when water leakage of a pipeline or water shortage in the heat exchanger is detected, alarm prompts are respectively carried out so as to ensure that maintenance personnel can timely collect message prompts.
When in use: as shown in figure 1, high temperature tail gas (110-, and at the same time, the speed of water circulation of the internal circulation pipeline is controlled, so that the temperature of the first heat exchange medium 8 is reduced to 70 ℃, and the temperature can be ensured not to be condensed but to have the highest heat exchange efficiency when the heat exchange is carried out with the high-temperature tail gas (110-; and the temperature of the second heat exchange medium 9 is raised to about 80 ℃, and the second heat exchange medium 9 can be guided into a water supply pipeline of the gas-fired boiler at the moment, so that the gas consumption of the gas-fired boiler is reduced, and the second heat exchange medium can also be guided into an urban heating pipeline to realize heating and can also be used for other purposes.
The waste heat recovery system has the following characteristics:
1. the heat recovery efficiency is high, the energy utilization rate of the gas boiler can be improved as much as possible, firstly, the temperature of the first heat exchange medium 8 in the first heat exchanger 1 is controlled to be as low as possible on the premise that the temperature is higher than the dew point and the first heat exchange medium is not easy to corrode, so that the heat exchange efficiency is higher when the first heat exchange is carried out on the first heat exchange medium and the tail gas; secondly, the first heat exchanger 1 adopts finned tubes with oval cross sections, and the heat exchange efficiency is further improved because the width of the finned tubes in the wind direction is wider on the premise of meeting the requirement of smaller wind resistance, and the heat exchange time is longer and the heat exchange area is larger; in addition, the first heat exchanger 1 does not condense, so that a heat exchanger with fins is selected, the heat exchange efficiency of the fins is high, and the heat recovery efficiency is improved; moreover, the first heat exchange medium 8 also realizes heat exchange with the second heat exchange medium 9 through the third heat exchanger 6, so that the temperature of the second heat exchange medium 9 serving as an output product is further increased, and the heat recovery efficiency is further improved; more importantly, the heated first heat exchange medium 8 is used as raw material water of the gas boiler, so that the fuel quantity required by the gas boiler when heating the first heat exchange medium 8 is obviously reduced compared with the fuel quantity required by the original cooling water used as raw material, namely, the energy dissipation during subsequent long-distance conveying is avoided, and the starting point temperature of the gas boiler during steam production is increased, so that the energy utilization rate is improved; therefore, the waste heat recovery system has high heat recovery efficiency, and can improve the energy utilization rate of the gas-fired boiler as much as possible.
2. The anti-corrosion and anti-wind channel blockage method comprises the steps that firstly, for a first heat exchanger 1, the temperature of a first heat exchange medium 8 in the first heat exchanger is adjusted to be higher than the dew point temperature of water vapor condensation in tail gas, so that the water vapor can not be condensed at the first heat exchanger 1, and the outer surface of the first heat exchanger 1 adopts common anti-corrosion schemes such as hot galvanizing or electroplating, so that the anti-corrosion purpose of the first heat exchanger 1 is realized, the finned tube heat exchanger made of common carbon steel can be selected safely, and no condensation can occur, so that no acid solution can be formed, the surface of the first heat exchanger 1 can not rust, and the problem of preventing the flue blockage is solved; secondly, for the second heat exchanger 5, because the second heat exchanger 5 is in a low-temperature region, and the temperature of the second heat exchange medium 9 in the second heat exchanger is low, the second heat exchanger 5 is a core region for condensation heat exchange, and a large amount of condensed water is inevitably generated on the outer surface of the second heat exchanger 5, so that a large amount of dilute nitric acid solution can be formed, therefore, the second heat exchanger 5 is a core region which is corroded, and the corrosion resistance of the second heat exchanger is good, and the second heat exchanger 5 is integrally made of corrosion-resistant materials such as stainless steel and the like to play a main corrosion resistance role; in addition, in order to prevent the acid solution from being accumulated on the surface of the second heat exchanger 5, a smooth-surface non-groove light pipe heat exchanger is selected, so that the acid solution cannot be accumulated on the surface of the heat exchanger for a long time; furthermore, in order to prevent the acidic solution from bonding to the surface of the second heat exchanger 5 after being combined with the dust, the spraying pipe 4 is arranged, and the water outlet 43 is also arranged at the lower part of the spraying pipe, so that the outer surface of the second heat exchanger 5 is regularly washed, the dust and the acidic solution are washed down and discharged from the water outlet 43, and the corrosion of the outer surface of the second heat exchanger 5 and the inner wall surface of the flue is avoided; the design of the above anticorrosion measures has the advantages of excellent anticorrosion and flue blockage prevention on the premise of low cost, simple structure and high heat exchange efficiency; the corrosion of the waste heat recovery device is mainly electrochemical corrosion, the contents of the discharged gases of various boilers and gas turbines are different, the environmental pressures are different, the dew points (condensation-generating temperatures) are different, when the temperature of a certain point of the heat exchange device is lower than the condensation temperature, dew condensation can be generated, so that the heat exchanger is corroded, all the temperatures of the heat exchanger are higher than the dew point temperature by controlling the temperature of a cold-side medium of the heat recovery device, and the heat recovery quantity of a common heat exchanger can be reduced to the maximum extent by using common materials.
On the basis of the two characteristics, the novel energy-saving environment-friendly energy-saving device has the advantages of long service life of products, long service life, good economical efficiency and capability of reducing the investment recovery period.
Embodiment 2 of the waste heat recovery system of the present invention: as shown in fig. 5, the difference from embodiment 1 is that a fourth heat exchanger 7 is further provided after the second heat exchanger 5 to solve the whitening problem, specifically: the fourth heat exchanger 7 is an air-water heat exchanger, and because condensation does not exist basically, the heat exchanger which is made of common carbon steel and is subjected to galvanizing treatment can be adopted to reduce the cost, the heat exchange medium in the fourth heat exchanger 7 is the second heat exchange medium 9, namely, a part of the second heat exchange medium 9 exchanges heat in the third heat exchanger 6 is led into the fourth heat exchanger 7, so that reverse heating, namely heat return for short, of the tail gas is realized, and the tail gas whitening effect can be realized after the heat return.
The working principle of the whitening here is as follows: after passing through the second heat exchanger 5, most of moisture in the tail gas is condensed and separated out, the temperature of the tail gas is about 40 ℃, if the tail gas is directly discharged through a chimney, because the temperature of the tail gas is lower (lower than the dew point), when the tail gas is contacted with the inner wall of the chimney, because the temperature of the inner wall of the chimney is lower, saturated water vapor can be further condensed, so that an acid solution can be generated on the inner wall of the chimney, the corrosion of the inner wall of the chimney is easily caused, and when the tail gas is positioned near a smoke exhaust port of the chimney, the tail gas is contacted with cold air and is condensed to form white fog; in the scheme, the fourth heat exchanger 7 is arranged behind the second heat exchanger 5, so that a part of the heated second heat exchange medium 9 can be guided to be heated by the tail gas, the temperature of the tail gas is higher than the dew point temperature, namely the temperature of the tail gas is higher than the dew point temperature when the tail gas is near the smoke exhaust port of the chimney and the smoke exhaust port of the chimney, condensation cannot occur, and after the tail gas is further diffused into the atmosphere, although the temperature of the tail gas is lower than the dew point temperature, the diffused water vapor is relatively dispersed, water mist cannot be formed, and therefore white mist cannot occur, and the purpose of whitening is achieved. According to the scheme, additional energy is not required to be utilized for heating the tail gas, the temperature of the tail gas is utilized to be reversely heated for the tail gas after heat exchange, and therefore whitening is achieved.
It should be noted that: in the scheme, the tail gas is heated to be higher than 60 ℃ through regenerative heating after being reduced from 150 ℃ to 40 ℃, the regenerative process is not a repeated process, and the scheme is different from the scheme that the tail gas is directly reduced from 150 ℃ to 60 ℃, because the tail gas is a large amount of condensation processes carried out at the second heat exchanger 5 in the process of reducing the temperature to 40 ℃, most of water vapor in the tail gas is condensed and separated out in the process, therefore, the air is only heated in the subsequent regenerative process, the energy consumption of heating is low, and the humidity of the tail gas can be effectively reduced. It can be seen that the reduction from 60 ℃ to 40 ℃ and the heating from 40 ℃ to 60 ℃ in this solution are irreversible processes, since the moisture content in the exhaust gas is different in the two processes, the former having a large energy variation, and the latter having a small energy variation due to the phase transition process involving little water. This is also an ingenious aspect of the present solution.
Through this scheme, can realize protecting rear end chimney internal face material not corroded, reduce the humidity of discharging fume, prevent that vapor from appearing, and realize taking off white. In addition, the scheme achieves the extreme effect of heat recovery, and increases the utilization rate of heat as much as possible on the premise of meeting the requirement of whitening.
In use, as shown in fig. 5, the difference from example 1 is that the second heat exchange medium 9 (about 80 ℃) having passed through the third heat exchanger 6 is not directly introduced into the steam boiler feed water, but the exhaust gas (40 ℃ and 100% humidity) is heated by the fourth heat exchanger 7 to obtain an exhaust gas temperature of about 50 ℃ and a humidity of about 70%, while the temperature of the second heat exchange medium 9 is lowered to about 75 ℃, and the second heat exchange medium 9 (about 75 ℃) is subsequently introduced into the steam boiler feed water.
Specific embodiments of the boiler system of the present invention: take gas boiler system as an example, the system includes boiler body, water softener, water tank, oxygen-eliminating device, steam-distributing cylinder, feed pump, oxygen pump, continuous blowdown flash tank, combustor, flue, pipeline and waste heat recovery system, and waste heat recovery system's specific structure is the same with the structure in the above-mentioned embodiment, no longer explains repeatedly.
The first embodiment described above was compared for operational economy:
(1) basic principle of thermodynamics:
by the chemical equation: CH4+2O2 is CO2+2H2O, and it is known that 1mol of methane is combusted, and 2mol of oxygen is consumed, and 1mol of carbon dioxide and 2mol of water vapor are produced.
According to the current field real-time measurement of the oxygen content of the flue gas to be 0.3 percent and the mole number of oxygen in the common ambient air to be 20.95 percent, the volume ratio of the natural gas at the inlet of the boiler to the air is about 1: 11.5.
(2) Original design and this application new thermal behavior after reforming transform design contrast:
the original design air-out temperature is 55 ℃, the air-out temperature after the new transformation of the application can be lower than 50 ℃, and the specific air-out temperature is shown in the following table:
| index (I)
|
Original design
|
The scheme of the application
|
Unit of
|
| Temperature of outlet air
|
55
|
50
|
℃
|
| Temperature of inlet air
|
155
|
155
|
℃
|
| Amount of condensate precipitated
|
0.31
|
0.74
|
Kg/s
|
| Sensible heat recovery
|
1622
|
1703
|
Kw
|
| Latent heat recovery
|
792.6
|
1893
|
Kw
|
| Total heat recovery
|
2414.6
|
3596.2
|
Kw
|
| Boiler energy efficiency
|
99.29
|
101.54
|
% |
As can be seen from the above table, the waste heat recovery system of the present application can recover 3596.2-2414.6 ═ 1181.6kw more than the waste heat recovery system in the original design ideal state, and the energy efficiency of the boiler after modification can reach 101.51% by bringing the newly added energy into the energy efficiency data of the original boiler.
(3) Performance comparison and investment cycle analysis before and after corresponding transformation of the application
At present, the air outlet temperature of the original equipment is 70 ℃, the air outlet temperature after the scheme of the application is transformed can be lower than 50 ℃, and the following concrete steps are as follows:
it can be seen from the above table that, according to the calculation of the current fuel utilization condition, the recovery and reconstruction investment cost can be realized within half a year through the fuel cost saved after the reconstruction in the state of 50% of the utilization rate of the boiler after the reconstruction.
(4) Analysis of overall waste heat recovery performance and economic benefit after transformation
The waste heat recovery pair at different inlet air temperatures after modification is as follows:
the specific embodiment of the waste heat recovery method of the invention comprises the following steps: the waste heat recovery method comprises the following steps: a first heat exchanger and a second heat exchanger for air-water heat exchange are sequentially arranged in the flue along the flow direction of flue gas, and the first heat exchanger and the second heat exchanger are respectively provided with a first internal pipeline and a second internal pipeline; a third heat exchanger is arranged outside the covering range of the flue gas, and the third heat exchanger is a water-water heat exchanger with a hot end pipeline and a cold end pipeline; the first internal pipeline is communicated with the hot end pipeline to form an internal circulation pipeline, a temperature detection module is arranged on the first internal pipeline, a first heat exchange medium is filled into the internal circulation pipeline, and a driving module is arranged to drive the first heat exchange medium to flow; connecting a cooling water outlet of the second internal pipeline with an inlet of the cold end pipeline through a water pipe, connecting a cooling water inlet of the second internal pipeline with a cooling water supply system, connecting an outlet of the cold end pipeline with a water inlet pipeline of the gas-fired boiler through a water pipe, and introducing a second heat exchange medium through the cooling water inlet; the setting controller is in control connection with the driving module and the temperature detection module, the temperature range is set through the controller, the set lowest temperature is higher than the dew point temperature of vapor in the flue gas when the vapor is condensed on the outer surface of the first heat exchanger, the set highest temperature is infinitely close to the lowest temperature so as to improve the heat exchange efficiency, the temperature of the first heat exchange medium detected by the temperature detection module is compared with the set temperature range, the driving module is controlled to operate slowly to reduce the flow of the first heat exchange medium when the detected actual temperature is lower than the set lowest temperature, and the driving module is controlled to operate quickly to improve the flow of the first heat exchange medium when the detected actual temperature is higher than the set highest temperature.
Wherein, first heat exchanger chooses for use the cross section to be oval first inside pipeline to arrange oval length direction along the flow direction of flue gas. The first heat exchanger is a finned tube heat exchanger. The driving module comprises a circulating water pump, and the circulating water pump is arranged on the inner circulating pipeline.
The above description is only a preferred embodiment of the present invention, and not intended to limit the present invention, the scope of the present invention is defined by the appended claims, and all structural changes that can be made by using the contents of the description and the drawings of the present invention are intended to be embraced therein.