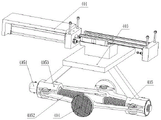
Automatic rolling, manufacturing and welding device for thin-wall steel plates
Technical Field
The invention relates to the technical field of machining and welding, in particular to an automatic rolling and welding device for thin-wall steel plates.
Background
The rolling machine is a production machine with high use frequency and wide popularization rate in domestic engineering production; the existing rolling machine which is used more generally is divided into a mechanical type and a hydraulic type, wherein the steel plate rolling machine has the advantages of small volume, low energy consumption, high efficiency and no noise. The device has the advantages of quick assembly, disassembly and use, simple operation, strong bearing capacity, long service life, quick rolling speed, multiple purposes, reliable quality and the like; however, most of the existing steel plate rolling machines are not butted with a welding device, and basically, the steel plate is transferred to a welding machine again for welding after rolling is finished, so that the defects that the elasticity profit stored in the steel plate after the rolling of the rolling machine is finished is not completely eliminated, and the rolled steel plate deforms to have errors in the process of butt welding machinery at the later stage, thereby affecting the quality of finished products;
patent numbers: CN110227947A discloses a metal winding machine production equipment, which comprises a metal plate positioning device and a welding robot; the metal plate positioning device comprises a support shaft, a cylinder body, a plurality of fixing rings and a driving assembly; the plurality of fixing rings are regularly arranged and sleeved on the supporting shaft; the outer ring of each fixing ring is provided with a fixing ring opening, a plurality of connecting rods are arranged between the outer rings of any two adjacent fixing rings, each connecting rod is arranged in parallel with the main shaft, the connecting rods are regularly arranged in a circular shape by taking the main shaft as a circle center, and the driving assembly is arranged on the connecting rods; the driving component is used for driving the free ends on the two sides of the opening of the fixing ring to be folded. The invention has the beneficial effects that the two free edges of the metal sheet are convenient to draw close and position, so that the welding is better carried out, the welding precision is improved, and the welding quality is improved.
Researches show that the overall efficiency of the device is slow, butt welding robots are needed for welding, the device is not integral, and the rolled thin plate still has the possibility of deformation in the process, so that a thin plate rolling and welding device is urgently needed to solve the problems.
Disclosure of Invention
Aiming at the problems, the invention provides an automatic rolling and welding device for thin-wall steel plates, which comprises: frame, centre gripping conveyer, its characterized in that: the device also comprises a primary rolling device, a secondary rolling device and a welding device; the clamping and conveying device is fixedly connected with the rack, and the primary rolling device, the secondary rolling device and the welding device are fixedly installed with the clamping and conveying device in sequence;
the clamping and conveying device is provided with a steel plate clamping jaw, the primary rolling device is provided with a positioning shaft group, and a steel plate is conveyed to the positioning shaft group through the steel plate clamping jaw; the secondary rolling device is provided with a propulsion cylinder and a secondary electromagnetic chuck, the propulsion cylinder controls the secondary electromagnetic chuck to move to reprocess the primarily rolled steel plate and move the primarily rolled steel plate to the welding device for welding through continuous control of the propulsion cylinder and the secondary electromagnetic chuck.
Further, the clamping and conveying device further comprises: the screw rod motor, the screw rod and the screw rod sliding block; the steel plate clamping jaw is fixedly connected with the lead screw sliding block.
Preferably, the clamping and conveying device is provided with a sliding rail, and the sliding rail is matched with the sliding block at the same time to guide and limit the movement of the thin-wall steel plate.
Further, the preliminary rolling device comprises a preliminary rolling bracket, a bevel gear disc and a preliminary rolling rod; the preliminary rounding support is fixedly arranged on a sliding rail, the number of the positioning shaft groups is two, the positioning shaft groups are fixedly arranged on the front surface and the rear surface of the preliminary rounding support, each positioning shaft group consists of two freely-rotating rollers, a roller rotating motor is arranged on each roller of the positioning shaft group arranged on the rear surface of the preliminary rounding support, and a thin-wall steel plate is fed from between the two rollers through the rotation of the roller rotating motor; the number of the bevel gear disks is two, the back surfaces of the bevel gear disks are fixedly connected in an attaching mode, a disk connecting shaft is fixed in the middle of each bevel gear disk, and the other end of each disk connecting shaft is fixed to the primary edge rolling support; the number of the primary winding rods is two, the primary winding rods are perpendicular to the sliding rails in the initial state and are connected to the front and the back of the bevel gear disc respectively, and the primary winding rods are provided with bevel gears and are connected with the bevel gear disc in a meshed mode.
Preferably, the primary winding bar is divided into an upper part and a lower part, and the upper part comprises: preliminary roll up pole motor, the lower part includes: the number of the bevel gears is two, the bevel gears are coaxially and fixedly connected with the primary winding rod motor and the axis of the primary electromagnetic chuck respectively, and the primary winding rod connecting rod is fixedly connected between the upper part and the lower part of the primary winding rod;
The preliminary electromagnetic chuck is used for adsorbing the center part of the fed steel plate, and the front and the back preliminary rolling rods rotate in different directions under the driving control of the front and the back preliminary rolling rod motors.
Further, the preliminary winding rod connecting rod is provided with a shaft sleeve which is rotatably connected with the disc connecting shaft and is used for supporting the rotation of the preliminary winding rod.
Preferably, the secondary rolling device further comprises: the secondary edge rolling machine comprises a secondary edge rolling machine frame, an electromagnetic chuck connecting frame and a chuck contraction device; the secondary edge rolling machine is characterized in that the secondary edge rolling machine frame is fixed on the upper surface of the machine frame, the propulsion cylinder is fixed between the lower surface of the secondary edge rolling machine frame and the electromagnetic chuck connecting frame, the chuck contraction device is fixed with the connecting rod of the electromagnetic chuck connecting frame, and the number of the secondary electromagnetic chucks is two, and the two secondary electromagnetic chucks are fixed on the outer side surfaces of two groups of hinged connecting rods in the chuck contraction device respectively.
Further, the suction cup retracting device further comprises: the device comprises a contraction motor, a contraction lead screw and a contraction sliding block; shrink motor and the coaxial fixed connection of shrink lead screw one end, shrink slider quantity is two and cooperates in shrink lead screw both ends, shrink lead screw both ends set up by opposite direction's screw thread, articulated connecting rod both ends are articulated with the same side of two shrink sliders.
Preferably, the welding device includes: welding the box body, the inner welding head and the outer welding head; the welding box body is fixedly connected to the sliding rail, a steel plate inlet and a steel plate outlet for rolling the steel plate in and out are formed in the front side face and the rear side face of the welding box body, an external welding port is formed in the upper surface of the welding box body, the internal welding head is fixed in the position, slightly lower than the position of a steel plate welding line, of the front side of the steel plate inlet of the welding box body through a support plate, and the external welding head is hinged to the position, close to the welding port, of the upper surface of the welding box body.
Compared with the prior art, the invention has the beneficial effects that:
in the invention, a rolling procedure is divided into two parts by the cooperation of two mechanisms of a primary rolling device and a secondary rolling device; firstly, a sheet steel can be preliminarily concave into a steel plate with a certain radian through a preliminary rolling device, and the steel plate with the certain radian is rolled again through a secondary electromagnetic chuck by a secondary rolling device; the two-step operation can reduce the error in one-step forming in the prior art and increase the machining precision.
In the invention, the final rolled steel plate is processed by matching the secondary rolling device and the welding device; after the coiling of the secondary coiling device is completed, the propulsion cylinder controls the secondary electromagnetic chuck to adsorb the coiled steel plate to feed to the inlet of the steel plate of the welding box body, the internal welding joint penetrates through the welding line to weld along with the feeding of the steel plate, the external welding joint welds from the welding port above the welding box body, the stress threat of the coiled steel plate at the moment is eliminated, and the deformation of the steel plate is avoided.
In the invention, the welding quality of the steel plate is ensured by welding the inner and outer welding heads of the welding device.
Drawings
FIG. 1 is a schematic internal three-dimensional view of the overall assembly structure of the present invention.
Fig. 2 is a three-dimensional schematic view of the final assembly structure of the present invention.
FIG. 3 is a three-dimensional schematic view of the bottom cleaning mechanism of the present invention.
FIG. 4 is a bottom two-dimensional schematic view of the bottom cleaning mechanism of the present invention.
FIG. 5 is a schematic view of the bottom cleaning mechanism according to the present invention.
Fig. 6 is a schematic structural diagram of the positioning device and the front plate feeding device of the present invention.
FIG. 7 is a three-dimensional schematic view of the overall mechanism of the upper surface cleaning mechanism of the present invention.
FIG. 8 is a three-dimensional schematic view of the interior of the upper surface cleaning mechanism of the present invention.
FIG. 9 is an enlarged view of a portion of the interior of the upper surface cleaning mechanism of the present invention.
Fig. 10 is a three-dimensional schematic diagram of the whole mechanism of the discharging device.
In the figure: 1-a frame; 2-a gripping and conveying device; 3-a preliminary rolling device; 4-secondary rolling device; 5-a welding device; 201-a slide rail; 203-lead screw motor; 204-a lead screw; 205-lead screw slider; 206-steel plate jaws; 301-positioning the shaft group; 3011-a roller rotation motor; 302-preliminary crimping of the stent; 303-a bevel gear disc; 3031-disc coupling; 304-primary winding rod; 3041-a primary winding motor; 3042-bevel gears; 3043-preliminary electromagnetic chuck; 3044-a preliminary rod-winding connecting rod; 401-propulsion cylinder; 402-a secondary rolling stand; 403-electromagnetic chuck connecting frame; 404-secondary electromagnetic chuck; 405-a suction cup retraction device; 4051-shrink motor; 4052-shrink screw; 4053-shrink slider; 501-welding a box body; 502-internal weld head; 503-external welding head.
Detailed Description
The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only a part of the embodiments of the present invention, and not all of the embodiments. In the embodiments of the present invention, all other embodiments obtained by workers in the field without creative efforts shall fall within the protection scope of the present invention.
Referring to fig. 1 to 10, the present invention provides a technical solution: the utility model provides an automatic book of thin-walled steel board makes welding set, includes: frame 1, centre gripping conveyer 2, its characterized in that: a primary rolling device 3, a secondary rolling device 4 and a welding device 5; the clamping and conveying device 2 is fixedly installed on the rack 1, and the primary rolling device 3, the secondary rolling device 4 and the welding device 5 are fixedly installed with the clamping and conveying device 2 according to the conveying direction of the clamping and conveying device 2 to the thin-wall steel plate;
the clamping and conveying device 2 is provided with a steel plate clamping jaw 206, the primary rolling device 3 is provided with a positioning shaft group 301, and the steel plate is conveyed to the positioning shaft group 301 through the steel plate clamping jaw 206 to complete the positioning of the steel plate; the secondary rolling device 4 is provided with a propulsion cylinder 401 and a secondary electromagnetic chuck 404, the propulsion cylinder 401 controls the secondary electromagnetic chuck 404 to move to reprocess the primarily rolled steel plate, and the propulsion cylinder 401 and the secondary electromagnetic chuck 404 move to the welding device 5 to weld through intermittent reciprocating motion.
In an optional implementation manner of the embodiment of the present invention, the clamping and conveying device 2 further includes: a screw motor 203, a screw 204 and a screw slider 205; the output shaft of the screw motor 203 is fixedly connected with the screw 204, the screw slider 205 is slidably mounted on the screw 204, and the steel plate clamping jaw 206 is fixedly connected with the screw slider 205, so that the purpose of controlling the screw slider 205 to slide on the screw 204 through the screw motor 203 so as to control the movement of a steel plate is achieved, and the stability and the control precision of the transportation process are greatly improved due to the transportation of the screw structure.
In another embodiment of the present invention, the clamping and conveying device 2 is provided with a slide rail 201, the slide rail 201 is matched with the slide block 205 at the same time, and the slide rail arranged on the slide rail 201 is matched with the slide block 205 to guide and limit the movement of the thin-walled steel plate and to be matched with a subsequent processing mechanism in a unified manner, so that the coordination of the machine is improved, and the azimuth error is reduced.
In another optional implementation manner of the embodiment of the present invention, the preliminary rolling device 3 includes a preliminary rolling support 302, a bevel gear disc 303, and a preliminary rolling rod 304; the primary rolling support 302 is fixedly arranged on the sliding rail 201, and the primary rolling support 302 can be fixedly arranged with the rack 1 under the action of fixed support, so that all fixed support steel structures are within a protection range without being taken as a limiting condition; the number of the positioning shaft groups 301 is two, the positioning shaft groups 301 are fixedly arranged on the front surface and the rear surface of the primary rolling support 302, each positioning shaft group 301 is composed of two freely-rotating rollers, a roller rotating motor 3011 is arranged on each roller of the positioning shaft group 301 arranged on the rear surface of the primary rolling support 302, the thin-walled steel plate is rolled from the positioning shaft group 301 in front through the steel plate clamping jaws 206 to correct and position the pitch angle, and the second positioning shaft group 301 bites into the thin-walled steel plate to position the thin-walled steel plate and drives the thin-walled steel plate to continuously feed forwards through the roller rotating motor 3011; the number of the bevel gear disks 303 is two, bevel gears face outwards, the back faces of the bevel gear disks are attached and fixed coaxially, a disk connecting shaft 3031 is fixed in the middle of each bevel gear disk 303, and the other end of each disk connecting shaft 3031 is fixed to the primary edge rolling support 302; the number of the primary winding rods 304 is two, the primary winding rods 304 are perpendicular to the sliding rail 201 in the initial state and are respectively connected to the front and the rear of the bevel gear disc 303, the primary winding rods 304 are provided with bevel gears 3042 which are in meshed connection with the bevel gear disc 303, and the arrangement enables the front and the rear primary winding rods 304 and the bevel gear disc 303 to rotate relatively stably and in opposite directions.
In an optional implementation manner of the embodiment of the present invention, the primary winding bar 304 is divided into an upper portion and a lower portion, and the upper portion includes: the preliminary winding bar motor 3041 includes, in the lower part: two primary electromagnetic chucks 3043 are provided, the number of the bevel gears 3042 is two, and the two bevel gears are respectively coaxially and fixedly connected with the axes of the primary winding rod motor 3041 and the primary electromagnetic chucks 3043, and the primary winding rod connecting rod 3044 is fixedly connected between the upper part and the lower part of the primary winding rod 304, so as to ensure the consistency of the rotation speed of the upper part and the lower part; the primary electromagnetic chuck 3043 is used for adsorbing the center of a fed steel plate, the front and rear primary winding rods 304 are driven and controlled by the front and rear primary winding rod motors 3041 to rotate in different directions, the primary electromagnetic chuck 3043 and the thin-wall steel plate are electromagnetically adsorbed in the rotating process, the thin-wall steel plate can slide on the thin-wall steel plate by controlling the current magnitude through the primary electromagnetic chuck 3043 and can be deformed by utilizing electromagnetic force, and the thin-wall steel plate is finally deformed into a standard arc because the rotating center and the length of the primary winding rod 304 are unchanged, and the thin-wall steel plate is previously fed under the action of the roller rotating motor 3011 and is separated from the second group of positioning shaft groups 301 immediately in the process; when the plane intersection angle between the front and rear primary winding bars 304 is less than 60 degrees, the rotation is stopped.
In another optional implementation manner of the embodiment of the present invention, the primary winding bar connecting rod 3044 is provided with a shaft sleeve rotatably connected to the disc connecting shaft 3031, and is used for supporting the rotation of the primary winding bar 304.
In an optional implementation manner of another embodiment of the present invention, the secondary rolling device 4 further includes: a secondary rolling machine frame 402, an electromagnetic chuck connecting frame 403 and a chuck contracting device 405; the secondary rolling rack 402 is fixed on the upper surface of the rack 1, the secondary rolling rack 402 has a fixing and supporting function on the secondary rolling device 4, and the fixing mode, specific shape and material of the secondary rolling rack are not used as conditions for limiting the protection scope of the invention; the propulsion cylinder 401 is fixed between the lower surface of the secondary edge rolling rack 402 and the electromagnetic chuck connecting frame 403, wherein the electromagnetic chuck connecting frame 403 is fixed at the propulsion end of the propulsion cylinder 401 and is controlled by the propulsion cylinder 401 to move, the chuck shrinking device 405 is fixed with the connecting rod of the electromagnetic chuck connecting frame 403, two secondary electromagnetic chucks 404 are respectively fixed at the outer side surfaces of two groups of hinged connecting rods 4054 in the chuck shrinking device 405, the electromagnetic chuck connecting frame 403 and the fixed connecting part thereof are controlled by the propulsion cylinder 401 to move, when the thin-walled steel plate is rolled by the primary edge rolling device 3, the propulsion cylinder 401 controls the chuck shrinking device 405 and the secondary electromagnetic chuck 404 to move forwards, and the secondary electromagnetic chuck 404 adsorbs the thin-walled steel plate; after the secondary rolling device 4 finishes rolling, the air cylinder 401 is pushed to control the suction cup contraction device 405 and the secondary electromagnetic suction cup 404 to move backwards, so that the rolled steel plate enters the welding device 5 for welding, and the feeding of the rolled steel plate is controlled through the repeated movement of the secondary electromagnetic suction cup 404.
In an optional implementation manner of the embodiment of the present invention, the suction cup retracting device 405 further includes: a shrinking motor 4051, a shrinking lead screw 4052 and a shrinking slider 4053; shrink motor 4051 and the coaxial axle center fixed connection of shrink lead screw 4052 one end, shrink slider 4053 quantity is two cooperations in shrink lead screw 4052 both ends, shrink lead screw 4052 both ends set up by opposite direction's screw, articulated connecting rod 4054 both ends are articulated with two same sides of shrink slider 4053.
In another optional implementation manner of the embodiment of the present invention, the welding device 5 includes: a welding box body 501, an inner welding head 502 and an outer welding head 503; the welding box body 501 is fixedly connected to the sliding rail 201, a steel plate inlet and a steel plate outlet used for rolling steel plates in and out are formed in the front side face and the rear side face of the welding box body 501, an external welding port is formed in the upper surface of the welding box body 501, the internal welding head 502 is fixed in the front of the steel plate inlet of the welding box body 501 through a support plate and is slightly lower than the position of a steel plate welding seam, the external welding head 503 is hinged to the position close to the welding port in the upper surface of the welding box body 501, the welding angle of the external welding head 503 on the welding box body 501 can be adjusted conveniently, and the welding quality can be controlled conveniently.
The working principle is as follows: the thin-wall steel plate is fixed on a steel plate clamping jaw 206 and is controlled by a screw motor 203 to be transmitted to a first group of positioning shaft groups 301, the thin-wall steel plate is positioned by the first group of positioning shaft groups 301 and then is driven by a second group of positioning shaft groups 301 to feed, and after the central position of the front part of the thin-wall steel plate is adsorbed by a primary electromagnetic chuck 3043, a front primary winding rod 304 and a rear primary winding rod 304 are driven by a primary winding rod motor 3041 to rotate on fixed shafts in opposite directions on a bevel gear disc 303; at this time, the thin-wall steel plate leaves the second group of positioning shaft groups 301, the thin-wall steel plate can slide on the thin-wall steel plate by controlling the current magnitude and can be deformed by utilizing electromagnetic force through the primary electromagnetic chuck 3043, and because the rotation center and the length of the primary winding rod 304 are unchanged, the thin-wall steel plate is finally deformed into a standard arc, and in the process, the thin-wall steel plate is fed in advance under the action of the roller rotation motor 3011 and is separated from the second group of positioning shaft groups 301 immediately; when the plane intersection angle between the front and the rear primary winding rods 304 is less than 60 degrees, stopping rotating; the propulsion cylinder 401 controls the sucker contraction device 405 and the secondary electromagnetic sucker 404 to move forwards, the secondary electromagnetic sucker 404 adsorbs the thin-wall steel plate and controls the contraction sliding block 4053 through the contraction motor 4051 so that the secondary electromagnetic sucker 404 adsorbs the primarily coiled steel plate to contract to complete secondary coiling; after the secondary rounding device 4 finishes rolling, the propulsion cylinder 401 controls the sucking disc contraction device 405 and the secondary electromagnetic sucking disc 404 to move backwards, so that a rolled steel plate enters the welding device 5 to be welded, the internal welding head 502 is located inside a welding seam of the rolled steel plate and is welded along with the forward movement process of the rolled steel plate, the rolled steel plate is sucked and fed forwards through the reciprocating motion of the propulsion cylinder 401 controlling the secondary electromagnetic sucking disc 404, and the external welding head 503 above the welding box body 501 welds the external welding seam of the rolled steel plate.
The foregoing shows and describes the general principles, essential features, and advantages of the invention. It will be understood by those skilled in the art that the present invention is not limited to the embodiments described above, and the preferred embodiments of the present invention are described in the above embodiments and the description, and are not intended to limit the present invention. The scope of the invention is defined by the appended claims and equivalents thereof.