Automatic door and window turning double-side gluing production line and processing method thereof
Technical Field
The invention relates to door and window gluing equipment, in particular to an automatic door and window gluing machine, and belongs to the technical field of mechanical equipment for building decoration.
Background
With the increase of the demand of commercial buildings and resident buildings in China, the demand of doors and windows of the building is increased year by year. At present, the door and window for the building in China mainly takes a rectangle and consists of glass and sectional materials, sealant needs to be coated or sealed between the glass and the sectional materials in the processing process, the sealing mode of the sealing strip has a plurality of defects, the mounting process of the sealing strip is complex, the sealing strip is easy to age, interfaces are arranged between the transverse sealing strip and the vertical sealing strip, the sealing effect is poor, and the sealing strip is gradually replaced by the mode of coating the sealant; the existing glue applying equipment is single-sided glue applying, the automation degree is relatively low, the glue can be transferred and transported after the glue has certain strength, the time consumption is long, the efficiency is low, and a large production field needs to be occupied. In order to improve the production efficiency, the existing gluing machine is improved by some people, for example, a patent of 201720471793.4 named as a double-sided door and window gluing machine, which is disclosed by the state intellectual property office in 2018, 3 and 2, by a canadian and a wary design, and comprises a door and window conveying device, a portal frame, an upper gluing unit and a lower gluing unit, wherein the portal frame is arranged above the door and window conveying device, the upper gluing unit is arranged on the portal frame, the lower gluing unit corresponding to the upper gluing unit is arranged below the door and window conveying device, glue valves for controlling glue outlet are arranged on the upper gluing unit and the lower gluing unit, the portal frame can move along an X axis under the driving of a walking gear, and the upper gluing unit and the lower gluing unit can move along a Y axis under the driving of an upper ball screw rod and a lower ball screw rod respectively; the upper gluing unit and the lower gluing unit can move along the Z axis and enable the gluing heads to rotate on the spot. However, the gluing machine with the structure has no product to be sold, and has more problems, such as the upper gluing unit and the lower gluing unit need to act simultaneously, synchronous control is not easy to carry out, the installation, debugging and use of the lower gluing unit are inconvenient, and the gluing quality cannot be observed and controlled visually.
The gluing equipment with high automation degree, stable gluing quality and simple structure becomes the urgent need equipment in the current building decoration industry.
Disclosure of Invention
The invention aims to provide an automatic door and window overturning double-sided gluing production line, which solves the problems of low production efficiency, high labor intensity, high loss, unstable gluing quality, single-sided gluing and low automation degree in the prior art.
The invention also provides a processing method for processing the door and window by utilizing the door and window automatic-overturning double-sided gluing production line.
The technical scheme adopted by the invention for realizing the purpose is as follows:
the utility model provides a two-sided production line of gluing of automatic upset of door and window which characterized in that: the automatic glue-applying machine comprises a feeding conveying device, a first automatic glue-applying machine, a turnover machine, a second automatic glue-applying machine, a discharging conveying device, a pneumatic system and an electric control system; the turnover machine can turn the door and the window 180 degrees.
Through adopting above-mentioned technical scheme, with feeding conveyor, beat the machine of glue, ejection of compact conveyor and arrange into the production line according to door and window and beat the order of gluing, set up the upset machine and can overturn 180 degrees doors and windows between first automatic gluing machine and the automatic gluing machine of second, can improve production efficiency greatly, use manpower sparingly, alleviate intensity of labour.
In the automatic door and window overturning double-sided gluing production line, the overturning machine comprises a left overturning device and a right overturning device, the left overturning device and the right overturning device have the same structure and comprise,
a turnover frame fixed on the foundation,
the door and window conveying device comprises at least 3 conveying rollers which are driven by a power and transmission mechanism to rotate and are arranged on the upper plane of the turnover frame,
a turnover support seat arranged on the side surface of the turnover frame,
a bearing seat which is arranged on the overturning support,
the turnover shaft is rotationally connected to the bearing seat through a bearing,
at least 2 turning frames, one end of each turning frame is connected to the turning shaft, each turning frame is positioned between two adjacent conveying rollers, the turning frames are in a horizontal position when being folded, the height of the turning frames is lower than the plane formed by the upper generatrices of the conveying rollers,
the door and window X-direction positioning plate is connected to the foremost turnover frame and is higher than the upper plane of the turnover frame; in the process of forward conveying of the doors and windows, the doors and windows are blocked when touching the X-direction positioning plate of the doors and windows, so that the doors and windows can be positioned in the X direction;
the door and window Y-direction positioning plate is arranged at one end of the turnover frame close to the turnover shaft and is higher than the upper plane of the turnover frame;
a rodless cylinder which is arranged at the lower part of the roll-over stand, a long groove which is communicated up and down is arranged on the roll-over stand, a sliding block of the rodless cylinder can slide in the long groove,
the compressing block is connected on the slide block of the rodless cylinder, the rodless cylinder drives the slide block and the compressing block to compress the door and the window on the Y-direction positioning plate of the door and the window,
the overturning cylinder is hinged to the overturning rack, the rod end of the overturning cylinder is hinged to the overturning frame, and the piston rod of the overturning cylinder extends out to drive the overturning frame to rotate around the axis of the overturning shaft so as to overturn the overturning frame from the horizontal position to the vertical position;
the left overturning device and the right overturning device are oppositely arranged in the Y direction, and one side of the left overturning device, which is provided with the transmission shaft, is close to one side of the right overturning device, which is provided with the transmission shaft; the X left turnover device and the right turnover device are arranged in a staggered mode, and 1 turnover frame of the left turnover device is located between 2 turnover frames of the right turnover device.
By adopting the technical scheme, the left turnover device and the right turnover device have the same structure, so that the processing and the maintenance can be facilitated, and the production cost of equipment can be reduced.
Furthermore, the turnover frames are provided with door and window Y-direction positioning plates, and all the door and window Y-direction positioning plates are positioned on the same straight line; the overturning frames are all provided with overturning cylinders.
Through adopting above-mentioned technical scheme, all be provided with door and window Y to the locating plate on every roll-over stand for the upset machine can adapt to the great door and window of size also can adapt to the less door and window of size.
Furthermore, the door and window X is equipped with photoelectric switch on to the locating plate.
By adopting the technical scheme, the door and window can be detected in time, and a triggering signal for stopping the door and window conveying device and clamping the door and window by the rodless cylinder is provided for the control system.
In the door and window automatic turning double-sided gluing production line, the feeding and conveying device comprises,
a feeding frame fixed on the foundation,
door and window conveyor, including at least 3 its rotation conveying roller of drive by power and drive mechanism drive, set up in the last plane of upset frame.
In the door and window automatic turning double-sided gluing production line, the discharging and conveying device comprises,
a discharging frame fixed on the foundation,
door and window conveyor, including at least 3 its rotation conveying roller of drive by power and drive mechanism drive, set up in the last plane of upset frame.
In the automatic double-sided gluing production line that overturns of foretell door and window, door and window conveyor be 3 at least brushless motorized pulley of direct current that the interval set up, brushless motorized pulley of direct current is in the same place conveying roller, power and drive mechanism integration.
Through adopting above-mentioned technical scheme, every brushless motorized pulley of direct current all operates independently, simple structure, simple to operate and be convenient for control.
In the automatic two-sided production line of gluing that overturns of foretell door and window, door and window conveyor can also adopt following technical scheme, including installing the speed reducer at the electrified machine of upset frame/feeding frame/play work or material rest one end, install drive sprocket on the output shaft of speed reducer, 3 at least conveying rollers rotate to be connected in the last plane of upset frame/feeding frame/play work or material rest, double driven sprocket is installed to conveying roller one end, the chain is connected drive sprocket with the driven sprocket on the conveying roller that is close to the speed reducer, driven sprocket on other each conveying roller passes through the chain and links to each other in proper order.
Through adopting above-mentioned technical scheme, can make door and window conveyor's cost lower.
The invention also provides a method for processing the door and window by utilizing the door and window automatic-overturning double-sided gluing production line, which comprises the following steps:
a) placing the assembled door and window on a conveying roller of a feeding and conveying device, and starting a power and transmission mechanism of the conveying roller by a control system to drive the conveying roller to rotate so as to convey the door and window to a first automatic gluing machine;
b) after a sensor on the first automatic gluing machine detects a door and a window, a conveying roller on the gluing machine stops rotating, a rodless cylinder drives a pressing device to press the door and the window, an edge inspection mechanism on a head of the gluing machine automatically inspects the edge, then glue is applied for a circle along the inner side of the door and the window, and the head is lifted after glue is applied; the conveying rollers convey the doors and the windows to the left turnover device;
c) the conveying roller on the left overturning device drives the door and window to move forwards, and the door and window moves to the X-direction positioning plate of the door and window to be positioned in the X direction; meanwhile, the door and window enters the photoelectric switch sensing range, the photoelectric switch sends a signal, the control system controls the action of the rodless cylinder to clamp the door and window, and the direct-current brushless electric roller stops rotating;
d) the control system controls the turning cylinder of the right turning device to act, and a piston rod of the turning cylinder extends out to drive the turning frame to rotate around the axis of the turning shaft, so that the turning frame is turned from a horizontal position to a vertical position to wait;
e) the control system controls the action of a turnover cylinder of the left turnover device, a piston rod of the turnover cylinder extends out to drive the turnover frame to rotate around the axis of the turnover shaft, so that the turnover frame is turned from a horizontal position to a vertical position;
f) the rodless cylinder of the right turning device acts to clamp the door and window, and the rodless cylinder of the left turning device acts to loosen the door and window;
g) the turnover cylinder of the right turnover device acts, a piston rod of the turnover cylinder retracts to drive the turnover frame to rotate around the axis of the turnover shaft, so that the turnover frame is turned over from a vertical position to a horizontal position, the door and window falls on a conveying roller of the right turnover device, and the door and window are conveyed to a second automatic gluing machine; meanwhile, the overturning cylinder of the left overturning device acts, and a piston rod of the overturning cylinder retracts to drive the overturning frame to rotate around the axis of the overturning shaft, so that the overturning frame is overturned from a vertical position to a horizontal position;
h) after a sensor on the second automatic gluing machine detects a door and a window, a conveying roller on the gluing machine stops rotating, a rodless cylinder drives a pressing device to press the door and the window, an edge inspection mechanism on a head of the gluing machine automatically inspects the edge, then glue is applied for a circle along the inner side of the door and the window, glue application on the other side of the door and the window is completed, after glue application is completed, the head is lifted, and the conveying roller conveys the door and the window to a discharging conveying device;
i) and manually taking the processed door and window out of the discharging and conveying device.
The invention has the beneficial effects that:
compared with the prior art, the door and window automatic-overturning double-sided gluing production line provided by the invention has the advantages that the feeding conveying device, the gluing machine and the discharging conveying device are arranged into the production line according to the door and window gluing sequence, and the door and window can be overturned for 180 degrees by arranging the overturning machine between the first automatic gluing machine and the second automatic gluing machine, so that the production efficiency can be greatly improved, the labor is saved, and the labor intensity is reduced. And the left turnover device and the right turnover device of the turnover machine have the same structure, so that the turnover machine is convenient to process and maintain, and the production cost of equipment can be reduced. The turnover machine is provided with a door and window Y-direction positioning plate on each turnover frame, so that the turnover machine can adapt to doors and windows with larger sizes and doors and windows with smaller sizes, and the machining range is wide. The production line can realize automatic operation, saves labor, can greatly improve the production efficiency, reduces the product disqualification rate, and has the advantages of convenient operation, low production cost, stable gluing quality and high product qualification rate.
Drawings
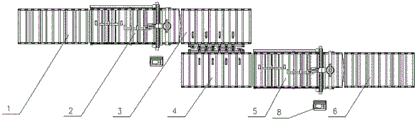
Fig. 1 is a schematic view of an automatic door and window turning double-sided gluing production line.
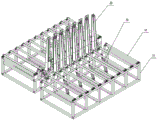
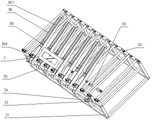
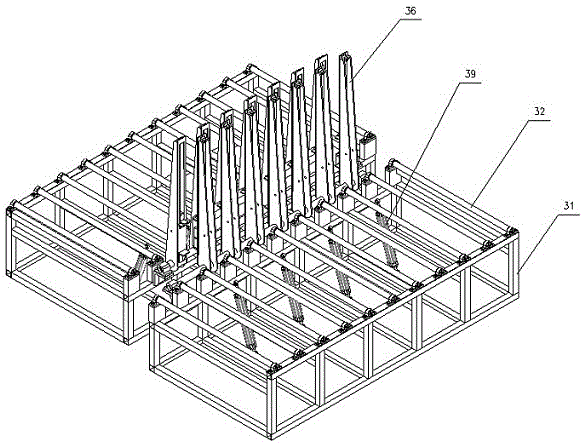
FIG. 2 is a schematic axial view of the tilter of the present invention.
Fig. 3 is a schematic top view of the upender of the present invention.
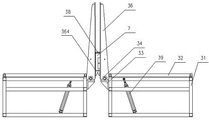
FIG. 4 is a side view of the inverting machine of the present invention.
Fig. 5 is a schematic diagram of the turning process of the left turning device in the invention.
Fig. 6 is a schematic view of the left turn-over device of the present invention turned over to a vertical state.
Fig. 7 is a schematic front side view of the left tilting device (a schematic connection view of the foremost tilting frame and the X-direction positioning plate of the door and window) in the present invention.
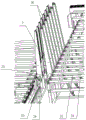
Fig. 8 is a schematic diagram of the left and right turners relaying a workpiece according to the present invention.
Fig. 9 is a schematic diagram of the turning process of the right turning device in the invention.
Fig. 10 is a schematic view of the right turn-over device of the present invention turned to a horizontal state.
Fig. 11 and 12 are schematic connection diagrams of the roll-over stand, the door and window Y-direction positioning plate, the rodless cylinder and the pressing block in the invention.
FIG. 13 is a schematic view of the feeding and discharging conveyor apparatus according to the present invention.
Fig. 14 and 15 are schematic diagrams of a first automatic gluing machine and a second automatic gluing machine according to the present invention.
In the figure: 1 a feeding and conveying device, 2 a first automatic gluing machine,
3 left turning device, 31 turning frame, 32 DC brushless electric roller, 33 turning support, 34 bearing seat, 35 turning shaft, 36 turning frame, 361 long groove, 362 door and window X direction positioning plate, 363 photoelectric switch, 364 door and window Y direction positioning plate, 37 rodless cylinder, 371 slide block, 38 pressing block, 39 turning cylinder,
4 right turning device, 5 automatic hits the machine of gluing of second, 6 ejection of compact conveyor, 7 doors and windows, 8 switch boards.
Detailed Description
In order to clearly illustrate the technical features of the present invention, the present invention is further illustrated by the following non-limiting examples in combination with the accompanying drawings.
The front, rear, left and right directions of the present invention are described with reference to the front, rear, left and right directions shown in the drawings. For ease of illustration, only the portions relevant to the embodiments of the present invention are shown.
The first embodiment is as follows:
referring to fig. 1 to 14, a door and window automatic turning double-sided gluing production line comprises a feeding conveying device 1, a first automatic gluing machine 2, a turning machine, a second automatic gluing machine 5, a discharging conveying device 6, a pneumatic system and an electric control system; the turnover machine comprises a left turnover device 3 and a right turnover device 4, the feeding and conveying device 1, a first automatic gluing machine 2, the left turnover device 3 is sequentially arranged into a first longitudinal column according to the advancing direction of a processed door window 7, the right turnover device 4, a second automatic gluing machine 5 and a discharging and conveying device 6 are sequentially arranged into a second longitudinal column according to the advancing direction of the processed door window 7, the first longitudinal column and the second longitudinal column are parallel to each other, the left turnover device 3 and the right turnover device 4 are identical in structure, can be connected with a force transmission door window, and can turn over the door window 7 by 180 degrees.
Left turning device 3 is the same with right turning device 4 structure, all including being fixed in the upset frame 31 on the ground, sets up in the planar door and window conveyor in the last of upset frame 31, and the door and window conveyor of this embodiment adopts the brushless motorized pulley 32 of direct current that is in the same place conveying roller, power and drive mechanism integration, according to the size of a dimension that needs processing door and window 7, selects the quantity of confirming brushless motorized pulley 32 of direct current, and this embodiment is 11, mutual equidistant arrangement. 2 overturning supports 33 are arranged on the side surface of the overturning frame 31, bearing seats 34 are arranged on the overturning supports 33, and overturning shafts 35 are rotatably connected to the bearing seats 34 through bearings. One end of 7 roll-over stands 36 is connected on trip shaft 35, every roll-over stand 36 is located between two DC brushless electric roller 32 adjacent to each other, roll-over stand 36 is in horizontal position when packing up, it is higher than the plane that the last generating line of DC brushless electric roller 32 constitutes, be connected with door and window X to locating plate 362 at the last plane of the foremost roll-over stand 36, door and window X is higher than the upper plane of roll-over stand 36 to locating plate 362, be equipped with the photoelectric switch mounting hole on door and window X is to locating plate 362, photoelectric switch 363 sets up in this mounting hole and links to each other with control system, can in time detect door and window 7, for control system provide door and window conveyor stop and the no pole cylinder 37 does the trigger signal of clamping door and window action, door and window X carries out X to locating plate 362 to door and window. A door and window Y-direction positioning plate 364 is arranged at one end, close to the turning shaft 35, of the turning frame 36, and the door and window Y-direction positioning plate 364 is higher than the upper plane of the turning frame 36; specifically, in this embodiment, a door and window Y-direction positioning plate 364 is disposed at one end of each roll-over stand 36 close to the roll-over shaft 35, the door and window Y-direction positioning plate 364 is mounted on the upper plane of the roll-over stand 36, and all the door and window Y-direction positioning plates 364 are located on a straight line in the X direction; the lower part of each roll-over stand 36 is provided with a rodless cylinder 37, the roll-over stand 36 is provided with a long groove 361 which is through up and down, a sliding block 371 of the rodless cylinder 37 can slide in the long groove 361, a pressing block 38 is connected to the sliding block 371 of the rodless cylinder 37, and the rodless cylinder 37 drives the sliding block 371 and the pressing block 38 to press the door and window 7 on a door and window Y-direction positioning plate 364. The lower part of the overturning frame 31 is hinged with an overturning cylinder 39, the rod end of the overturning cylinder 39 is hinged on the overturning frame 36, and the piston rod of the overturning cylinder 39 extends out to drive the overturning frame 36 to rotate around the axis of the overturning shaft 35, so that the overturning frame 36 overturns from the horizontal position to the vertical position; in order to adapt to the doors and windows 7 with larger sizes and improve the overturning reliability, each overturning frame 36 is provided with an overturning cylinder 39.
The left turnover device 3 and the right turnover device 4 are oppositely arranged in the Y direction, and one side of the left turnover device 3, which is provided with a transmission shaft, is close to one side of the right turnover device 4, which is provided with the transmission shaft; in the X direction, the left turning device 3 and the right turning device 4 are arranged in a staggered manner, and 1 turning frame 36 of the left turning device 3 is located between 2 turning frames 36 of the right turning device 4.
Feeding conveyor 1 sets up planar door and window conveyor on the feeding frame including being fixed in the feeding frame on the ground, and the door and window conveyor of this embodiment adopts the brushless motorized pulley of direct current who integrates conveying roller, power and drive mechanism together, according to the size of a dimension that needs processing door and window 7, selects the quantity of confirming the brushless motorized pulley of direct current, and this embodiment is 11, and equidistant each other arranges.
Ejection of compact conveyor 6 sets up in the planar door and window conveyor on the play work or material rest including being fixed in the foundation, and the door and window conveyor of this embodiment adopts the brushless motorized pulley of direct current who integrates conveying roller, power and drive mechanism together, according to the size of a dimension that needs processing door and window 7, selects the quantity of confirming the brushless motorized pulley of direct current, and this embodiment is 11, and equidistant each other arranges.
The first automatic gluing machine 2 is the same as the second automatic gluing machine 5 in structure and is a single-sided automatic gluing machine in the prior art, after a sensor on the single-sided automatic gluing machine detects a door and a window 7, a roller on the gluing machine stops rotating, a rodless cylinder compresses the door and the window 7, an edge inspection mechanism on a head of the gluing machine automatically inspects the edge, then the glue is applied for a circle along the inner side of the door and the window 7, and the head rises after the glue is applied. And the conveying rollers on the gluing machine convey the doors and windows to the left turnover device 3.
Example two:
a method for processing doors and windows by utilizing the automatic door and window overturning double-sided gluing production line comprises the following steps:
1. placing the assembled door and window 7 on a direct-current brushless electric roller 32 of the feeding and conveying device 1, and starting the direct-current brushless electric roller 32 to rotate by a control system to convey the door and window 7 to the first automatic gluing machine 2;
2. after a sensor on the first automatic gluing machine 2 detects a door and a window 7, a conveying roller on the gluing machine stops rotating, a rodless cylinder 37 drives a pressing device to press the door and the window 7, an edge inspection mechanism on a head of the gluing machine automatically inspects the edge, then glue is applied for a circle along the inner side of the door and the window 7, and the head is lifted after glue application; the conveying rollers convey the door and window 7 to the left turnover device 3;
3. the direct-current brushless electric roller 32 on the left turnover device 3 drives the door and window 7 to move forwards, and the door and window 7 moves to the door and window X-direction positioning plate 362 to perform X-direction positioning; meanwhile, the door and window 7 enters the sensing range of the photoelectric switch 363, the photoelectric switch 363 sends a signal, the control system controls the action of the rodless cylinder 37 to clamp the door and window 7, and the direct-current brushless electric roller 32 stops rotating;
4. the control system controls the action of the overturning cylinder 39 of the right overturning device 4, and the piston rod of the overturning cylinder 39 extends out to drive the overturning frame 36 to rotate around the axis of the overturning shaft 35, so that the overturning frame 36 overturns from the horizontal position to the vertical position to wait;
5. the control system controls the action of the overturning cylinder 39 of the left overturning device 3, and the piston rod of the overturning cylinder 39 extends out to drive the overturning frame 36 to rotate around the axis of the overturning shaft 35, so that the overturning frame 36 overturns from the horizontal position to the vertical position;
6. the rodless cylinder 37 of the right turning device 4 acts to clamp the door and window 7, and the rodless cylinder 37 of the left turning device 3 acts to loosen the door and window 7;
7. the turning cylinder 39 of the right turning device 4 acts, the piston rod of the turning cylinder 39 retracts to drive the turning frame 36 to rotate around the axis of the turning shaft 35, so that the turning frame 36 is turned from the vertical position to the horizontal position, the door and window 7 falls on the direct-current brushless electric roller 32 of the right turning device 4, and the door and window 7 is conveyed to the second automatic gluing machine 5; meanwhile, the turning cylinder 39 of the left turning device 3 acts, the piston rod of the turning cylinder 39 retracts to drive the turning frame 36 to rotate around the axis of the turning shaft 35, so that the turning frame 36 is turned from the vertical position to the horizontal position;
8. after a sensor on the second automatic gluing machine 5 detects a door and a window 7, a conveying roller on the gluing machine stops rotating, a rodless cylinder 37 drives a pressing device to press the door and the window 7, an edge inspection mechanism on a head of the gluing machine automatically inspects the edge, then a circle of glue is applied along the inner side of the door and the window 7, the other side of the door and the window 7 is glued, after the glue is applied, the head is lifted, and the conveying roller conveys the door and the window 7 to a discharging and conveying device 6;
9. and manually taking the processed door and window 7 out of the discharging and conveying device 6.
Example three:
the utility model provides a two-sided production line of gluing of automatic upset of door and window, its door and window conveyor is including installing the speed reducer of taking the motor in upset frame 31/feeding frame/play work or material rest one end, install drive sprocket on the output shaft of speed reducer, 3 at least conveying rollers rotate to be connected in the last plane of upset frame 31/feeding frame/play work or material rest, double driven sprocket is installed to conveying roller one end, the chain is connected drive sprocket with the driven sprocket on the conveying roller that is close to the speed reducer, driven sprocket on other each conveying roller passes through the chain and links to each other in proper order. The rest of the structure is the same as the first embodiment.
In the description of the present invention, it should be noted that the terms "left", "right", "front", "back", "upper", "lower", "inner", "outer", etc., indicate orientations or positional relationships based on those shown in the drawings, and the above terms are only for convenience in describing the present invention and simplifying the description, but do not indicate or imply that the device or element referred to must have a specific orientation, be constructed in a specific orientation, and be operated, and thus, should not be construed as limiting the present invention.
Unless expressly stated or limited otherwise, the terms "mounted," "connected," and "connected" are intended to be inclusive and mean, for example, that they may be fixedly connected, detachably connected, or integrally connected; they may be connected directly or indirectly through intervening media, or they may be interconnected between two elements. The specific meanings of the above terms in the present invention can be understood in specific cases to those skilled in the art.
In addition to the technical features described in the specification, the technology is known to those skilled in the art.
The above-mentioned embodiments are only for understanding the present invention, and are not intended to limit the technical solutions of the present invention, and those skilled in the art can make various changes or modifications based on the technical solutions described in the claims, and all equivalent changes or modifications should be covered by the scope of the claims of the present invention.