Four-process plate-tube heat exchanger and use method thereof
Technical Field
The invention relates to the technical field of heat exchange equipment, in particular to a four-flow plate-tube heat exchanger and a using method thereof.
Background
A heat exchanger (also called heat exchanger) is a device that transfers part of the heat of a hot fluid to a cold fluid. The heat exchanger plays an important role in chemical industry, petroleum industry, power industry, food industry and other industrial production, can be used as a heater, a cooler, a condenser, an evaporator, a reboiler and the like in chemical industry production, and is widely applied.
At present, the heat exchanger that uses now can not guarantee abundant heat transfer to the heat transfer process that has the phase transition, and accurate accuse temperature even is double-flow journey tube sheet heat exchanger, because same coolant liquid is used in board side and the heat transfer of tube side, so can not need a plurality of heat exchangers to connect in parallel or establish ties to the accurate accuse temperature of the liquid that flows, and continuous operation just can accomplish to whole heat transfer system whole cost and occupation space's increase has been brought.
Therefore, how to provide a four-flow plate-tube heat exchanger and a using method thereof are problems to be solved urgently by those skilled in the art.
Disclosure of Invention
In view of the above, the invention provides a four-flow plate-tube heat exchanger and a use method thereof, wherein a circulating cooling liquid and a low-temperature cooling liquid are adopted in one heat exchanger to perform heat exchange condensation and cooling on a phase-changeable fluid, so that not only can the space be saved and the heat exchange efficiency be improved, but also the temperature of the flowing condensed liquid can be accurately controlled by controlling the exchange area of a plate pass and a tube pass and the temperature and the flow of the two cooling liquids.
In order to achieve the purpose, the invention adopts the following technical scheme:
a four-flow plate-tube heat exchanger comprises a cylinder, wherein end plates are fixed at two ends of the cylinder to form a heat exchanger shell; a partition board is fixed in the shell along the axial direction of the shell, and the shell is divided into a plate-pass heat exchange cavity and a tube-pass heat exchange cavity by the partition board; a plurality of heat exchange plates are arranged in the plate pass heat exchange cavity in parallel with the end plate; the heat exchange plate sheets and the end plates are respectively provided with four through holes, the through holes are fixedly penetrated through fluid collecting and distributing inlet and outlet pipes, the heat exchange plate sheets, the end plates, the cylinders and the partition plates jointly form a plurality of small cavities, and two fluid collecting and distributing holes in the fluid collecting and distributing inlet and outlet pipes leak out of each small cavity, so that a phase-changeable gas condensation cavity and a cooling liquid cavity which are alternate are formed; a plurality of heat exchange tubes are vertically and fixedly arranged in the tube side heat exchange cavity and the end plates, and holes are formed in the cylinder close to the two end plates and fixedly connected with a low-temperature cooling liquid inflow tube and a low-temperature cooling liquid outflow tube; two ends of the cylinder, which correspond to the tube pass heat exchange cavity, are fixed with half end sockets, two ends of the heat exchange tubes penetrate through the end plate and are communicated with the inner cavity of the half end socket, and the half end sockets on two sides are respectively connected with a condensate inflow tube and a cooling condensate outflow tube; and the condensate inflow pipe is communicated with one of the fluid distribution inlet and outlet pipes.
The invention discloses a four-flow plate-tube heat exchanger, which is characterized in that phase-changeable gas is condensed after heat exchange in a plate-pass heat exchange cavity, condensed liquid enters the tube-pass heat exchange cavity for heat exchange, and finally flows out from a cooling condensate outflow tube; but phase transition gas has adopted recirculated cooling liquid and cryogenic cooling liquid to carry out heat transfer condensation and cooling to phase transition fluid in a heat exchanger, not only can practice thrift the space, improves heat exchange efficiency, moreover, through controlling temperature, the flow of control board side and tube side exchange area and two kinds of coolant liquids to the temperature of the condensed liquid that can accurate control flows out.
Preferably, four through holes formed in the heat exchange plate and the end plate are respectively an air flow hole, a condensate outflow hole, a coolant inflow hole and a coolant outflow hole, and fluid collecting and distributing inlet and outlet pipes respectively corresponding to and penetrating through the air flow hole, the condensate outflow hole, the coolant inflow hole and the coolant outflow hole are respectively a gas inflow pipe, a condensate outflow pipe, a coolant inflow pipe and a coolant outflow pipe; the condensate outflow pipe is communicated with the condensate inflow pipe through a connecting pipe.
The technical scheme has the advantages that four pipes with different use functions, namely the gas inflow pipe, the condensate outflow pipe, the cooling liquid inflow pipe and the cooling liquid outflow pipe, are all completed by the fluid collecting and distributing inflow and outflow pipes and are used in pairs, and the fluid collecting and distributing holes of each pair of pipes are just staggered with the fluid collecting and distributing holes of the other pair of pipes; the gas inflow pipe and the condensate outflow pipe are paired, and the coolant inflow pipe and the coolant outflow pipe are paired to urge the phase-change gas condensation chamber and the coolant chamber, respectively.
Preferably, the fluid dispersion holes have a diameter equal to the spacing distance.
The beneficial effect who adopts above-mentioned technical scheme is that, fluid collection and distribution hole evenly distributed for the heat transfer is more even.
Preferably, the spacing between adjacent fluid collection holes is at least greater than the thickness of the heat exchanger plates.
Adopt above-mentioned technical scheme's beneficial effect to but ensure that phase transition gas condensation chamber and coolant liquid chamber form independent cavity.
Preferably, the heat exchange tube is provided with an upper guide plate and a lower guide plate which are vertical to the heat exchange tube, and the lowest end of the upper guide plate is lower than the highest end of the lower guide plate.
The beneficial effect who adopts above-mentioned technical scheme is to make the cryogenic cooling liquid can distribute tube side heat transfer intracavity portion uniformly, guarantee that the heat transfer is even.
Preferably, the half end sockets are fixed at two ends of the cylinder through an inner flange, an outer flange, bolts and nuts, and the fixed positions of the half end sockets are located at the outer sides of the end plates corresponding to the tube side heat exchange cavities; and a half seal head gasket is arranged between the half seal head and the end plate.
Adopt above-mentioned technical scheme's beneficial effect be, interior flange, outer flange, bolt and nut can guarantee to be connected between half head and the end plate firmly, and half head gasket can prevent that the condensate in the half head from leaking outward.
Preferably, the half head is a semicircular arc body with an inner cavity and comprises an arc-shaped part and a flat plate part, and the arc-shaped part is provided with a condensate inlet and a condensate outlet.
The technical scheme has the beneficial effects that the condensed liquid in the heat exchange tube can be conveniently collected and then flows out through the cooling condensed liquid outflow tube.
Preferably, the partition plate is welded and fixed to the cylinder, and both ends of the connecting pipe are welded and fixed to the condensate outflow pipe and the condensate inflow pipe, respectively.
By adopting the technical scheme, the welding fixture has the advantages of firm welding fixation and simple process.
Preferably, the end plate is provided with a plurality of heat exchange tube holes corresponding to the heat exchange tubes, and the fluid collecting and dispersing holes are square holes or round holes.
The technical scheme has the beneficial effects that the plurality of heat exchange tube holes are used for enabling the condensate in the heat exchange tubes to flow into the inner cavity of the half end enclosure; the shape of the fluid dispersion holes can be freely selected according to actual needs.
The invention also discloses a using method of the four-process plate-tube heat exchanger, after the phase-changeable gas enters the plate-pass heat exchange cavity from the gas inflow tube, the phase-changeable gas enters the plate-pass heat exchange cavity to be condensed due to the mutual alternate arrangement of the cooling liquid cavity and the phase-changeable gas condensation cavity, the condensed liquid enters the tube-pass heat exchanger through the condensate outflow tube, the connecting tube and the condensate inflow tube to exchange heat, and finally flows out from the cooling condensate outflow tube.
According to the technical scheme, compared with the prior art, the four-flow plate-tube heat exchanger and the using method thereof can be used for performing heat exchange condensation and cooling on the phase-changeable fluid by simultaneously adopting the circulating cooling liquid and the low-temperature cooling liquid in one heat exchanger, so that not only can the space be saved and the heat exchange efficiency be improved, but also the temperature of the flowing condensed liquid can be accurately controlled by controlling the exchange areas of the plate side and the tube side and the temperature and the flow of the two cooling liquids.
Drawings
In order to more clearly illustrate the embodiments of the present invention or the technical solutions in the prior art, the drawings used in the description of the embodiments or the prior art will be briefly described below, it is obvious that the drawings in the following description are only embodiments of the present invention, and for those skilled in the art, other drawings can be obtained according to the provided drawings without creative efforts.
Fig. 1 is a schematic external view of a four-flow-plate tube heat exchanger provided by the present invention.
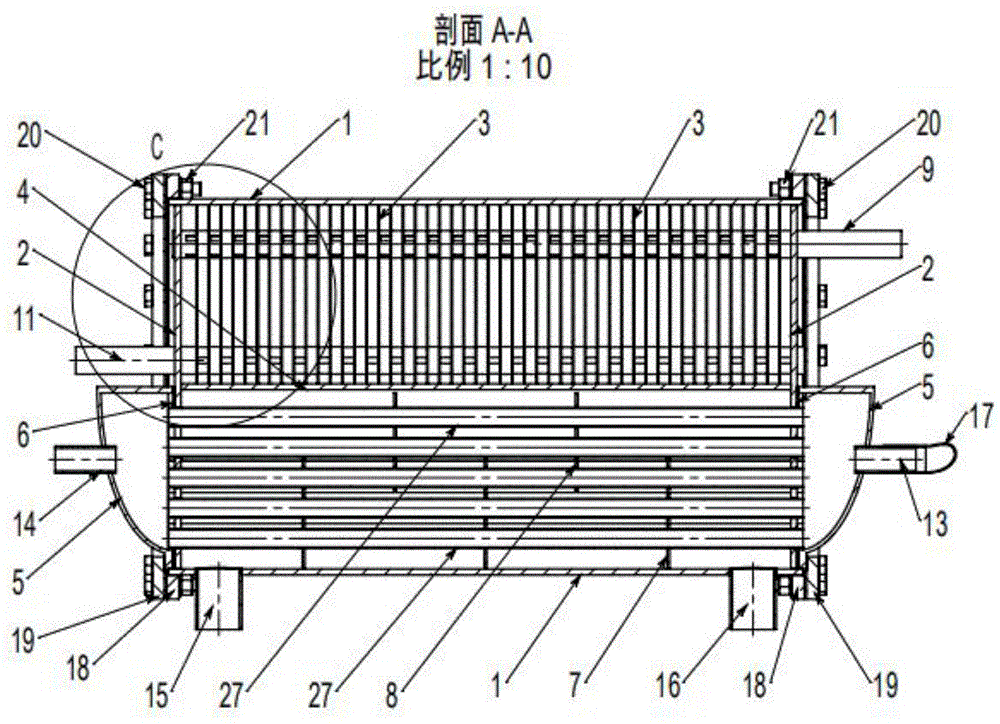
Fig. 2 is a schematic diagram of the internal structure of the four-flow-plate tube heat exchanger provided by the invention.
Fig. 3 is a schematic side view of a four-pass plate-tube heat exchanger according to the present invention.
Fig. 4 is a schematic diagram of fluid flow heat exchange in a heat exchanger by four fluids provided by the present invention.
Fig. 5 is a schematic view of a heat exchanger plate according to the present invention.
Fig. 6 is a schematic view of a fluid distribution inlet/outlet pipe provided by the present invention.
Fig. 7 is a schematic view of a half head provided by the invention.
Fig. 8 is a partial enlarged view of the internal structure of the plate-side heat exchange cavity provided by the invention.
Fig. 9 is a schematic view of an end plate provided by the present invention.
Wherein the reference symbols are:
1-cylinder, 2-end plate, 3-heat exchange plate, 4-clapboard, 5-half end enclosure, 6-end enclosure gasket, 7-lower guide plate, 8-upper guide plate, 9-gas inflow pipe, 10-condensate outflow pipe, 11-coolant inflow pipe, 12-coolant outflow pipe, 13-condensate inflow pipe, 14-cooling condensate outflow pipe, 15-low-temperature coolant inflow pipe, 16-low-temperature coolant outflow pipe, 17-connecting pipe, 18-inner flange, 19-outer flange, 20 bolt, 21 nut, 22-airflow hole, 23-condensate outflow hole, 24-coolant inflow hole, 25-coolant outflow hole, 26-fluid collecting and dispersing inflow pipe, 27-heat exchange pipe, 28-fluid collecting and dispersing hole, 29-outside of the half end socket flange, 30-inside of the half end socket flange, 31-phase-changeable gas condensation cavity, 32-cooling liquid cavity, 33-condensate inlet and outlet, 34-heat exchange tube hole, 51-arc part and 52-flat part.
Detailed Description
The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only a part of the embodiments of the present invention, and not all of the embodiments. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
As can be seen from fig. 1, 2, 3, and 4, an embodiment of the present invention discloses a four-flow plate-tube heat exchanger, including: the heat exchanger comprises a cylinder 1, an end plate 2, heat exchange plates 3, a partition plate 4, a half seal head 5, a half seal head gasket 6, a lower guide plate 7, an upper guide plate 8, a gas inflow pipe 9, a condensate outflow pipe 10, a cooling liquid inflow pipe 11, a cooling liquid outflow pipe 12, a condensate inflow pipe 13, a cooling condensate outflow pipe 14, a low-temperature cooling liquid inflow pipe 15, a low-temperature cooling liquid outflow pipe 16, a connecting pipe 17, an inner flange 18, an outer flange 19, a fluid collecting and distributing inflow pipe 26 and a heat exchange pipe 27. The two ends of the cylinder 1 are both fixed with end plates 2 to form a heat exchanger shell; a partition plate 4 is fixed in the shell along the axial direction of the shell, and the shell is divided into a plate pass heat exchange cavity and a tube pass heat exchange cavity by the partition plate 4; a plurality of heat exchange plates 3 are arranged in the plate pass heat exchange cavity and parallel to the end plate 2; the heat exchange plate 4 and the end plate 5 are respectively provided with four through holes, the through holes are fixedly penetrated through the fluid collecting and distributing inlet and outlet pipes 26, the heat exchange plate 3, the end plate 2, the cylinder 1 and the partition plate 4 jointly form a plurality of small cavities, and two fluid collecting and distributing holes 28 on the fluid collecting and distributing inlet and outlet pipes 26 leak out from each small cavity, so that a phase-changeable gas condensation cavity and a cooling liquid cavity which are alternate are formed;
a plurality of heat exchange tubes 27 are fixedly arranged in the tube side heat exchange cavity and are vertical to the end plates 2, and the cylinder 1 is provided with holes close to the two end plates 2 and is fixedly connected with a low-temperature cooling liquid inflow tube 15 and a low-temperature cooling liquid outflow tube 16; two ends of the cylinder 1 corresponding to the tube pass heat exchange cavity are fixed with half seal heads 5, two ends of a plurality of heat exchange tubes 27 penetrate through the end plate 2 to be communicated with the inner cavity of the half seal heads 5, and the half seal heads on two sides are respectively connected with a condensate inflow tube 13 and a cooling condensate outflow tube 14; and the condensate inflow pipe 13 communicates with one of the fluid-collecting inflow and outflow pipes 26.
The specific implementation of the four-flow plate-tube heat exchanger is as follows: first welded end plate 2 at 1 both ends of drum to form the heat exchanger casing, welding baffle 4 in the casing, divide into two cavitys with the casing, be board journey heat transfer chamber and tube side heat transfer chamber respectively, with end plate 2 parallel arrangement at least three above heat transfer slab 3 in one of them cavity, form board journey heat transfer chamber: in the other cavity, a plurality of heat exchange tubes 27 are arranged perpendicular to the end plate 2, and both ends of each heat exchange tube 27 are welded and fixed with the end plates 2 at both ends of the cylinder 1, so that a tube side heat exchange cavity is formed.
Next, referring to fig. 5 and 9, four holes with the same diameter, namely, an air flow hole 22, a condensate outflow hole 23, a coolant inflow hole 24, and a coolant outflow hole 25, are respectively formed in the two end plates 2 and all the heat exchanger plates 3, the four holes in all the heat exchanger plates 3 are respectively welded to four fluid collecting and distributing inflow and outflow pipes 26, and the heat exchanger plates are welded to the inner wall of the cylinder 1 and one side of the partition plate 4.
Further, as shown in fig. 8, the plate-side heat exchange cavity is a plurality of small cavities formed by a plurality of heat exchange plates 3, fluid collecting and distributing inlet and outlet pipes 26, a cylinder 1 and partition plates 4, and only two fluid collecting and distributing holes 28 on the fluid collecting and distributing inlet and outlet pipes 26 can leak out of each small cavity, so that a phase-changeable gas condensation cavity 31 and a cooling liquid cavity 32 which are arranged alternately are formed.
Further, as shown in fig. 6, the fluid collecting and distributing inlet and outlet pipes 26 have one end thereof blocked, and fluid collecting and distributing holes 28 are uniformly formed along the length direction of the pipes at intervals, preferably, the hole diameter is equal to the interval distance, and may be circular holes or polygonal holes, preferably square holes, and the interval between adjacent holes is at least larger than the thickness of the heat exchange plate 3. The pore diameter and the pore distance are determined by heat exchange balance calculation.
Further, referring to fig. 2 and 9, the tube side heat exchange cavity is formed by opening two holes on the side of the cylinder 1 near the two end plates 2 and welding a low-temperature coolant inflow tube 15 and a low-temperature coolant outflow tube 16, and a plurality of upper guide plates 8 and lower guide plates 7 are arranged on a plurality of heat exchange tubes 27.
Further, referring to fig. 1, 2 and 7, the two half heads 5 are respectively fixed by inner flanges 18 welded at both ends of the cylinder 1 and by outer flanges 19, bolts 20 and nuts 21, and the fixed positions are outside the end plates 2 corresponding to the tube side heat exchange cavities. As shown in fig. 7, the half head 5 is a moving semicircular arc body with an inner cavity, and includes an arc portion 51 and a flat plate portion 52, and the installation mode is that the outer surface 29 of the half head flange is close to the outer flange 19, the inner surface 30 of the half head flange is close to the inner flange 18, the arc portion 51 is provided with a condensate inlet and outlet 33, and the condensate inlet and outlet 33 is respectively communicated with the condensate inflow pipe 13 and the cooling condensate outflow pipe 14. And a half seal head gasket 6 is arranged between the half seal head 5 and the end plate 2. And a condensate inflow pipe 13 and a cooling condensate outflow pipe 14 are welded on the outer sides of the two half sealing heads 5.
Still further, a connecting pipe 17 is welded between the condensate outflow pipe 10 and the condensate inflow pipe 13.
It should be further noted that the four tubes having different functions of the gas inlet tube 9, the condensate outlet tube 10, the coolant inlet tube 11, and the coolant outlet tube 12 are all formed by the fluid collecting/discharging tubes 26, and are used only in pairs, with the fluid collecting/discharging holes 28 of each pair being offset from those of the other pair.
The invention discloses a four-flow plate-tube heat exchanger, which comprises the following use processes: but phase transition gas gets into behind the board journey heat transfer chamber from gas inflow pipe 9, because coolant liquid chamber 32 and the looks alternate arrangement each other of phase transition gas condensation chamber 31, but phase transition gas gets into behind the board journey heat transfer chamber and is condensed, liquid after the condensation passes through condensate outflow pipe 10, connecting pipe 17 and condensate inflow pipe 13 get into the tube side heat exchanger and carry out the heat transfer, flow out from cooling condensate outflow pipe 14 at last, but realize adopting recirculated cooling liquid and cryogenic cooling liquid to carry out the heat transfer condensation and cooling to phase transition fluid in same heat exchanger simultaneously, not only practice thrift the space, improve heat exchange efficiency, moreover, the exchange area and the temperature of two kinds of coolant liquids through control board journey and tube side, the flow, thereby can the temperature of the condensed liquid that accurate control flows.
The embodiments in the present description are described in a progressive manner, each embodiment focuses on differences from other embodiments, and the same and similar parts among the embodiments are referred to each other. The device disclosed by the embodiment corresponds to the method disclosed by the embodiment, so that the description is simple, and the relevant points can be referred to the method part for description.
The previous description of the disclosed embodiments is provided to enable any person skilled in the art to make or use the present invention. Various modifications to these embodiments will be readily apparent to those skilled in the art, and the generic principles defined herein may be applied to other embodiments without departing from the spirit or scope of the invention. Thus, the present invention is not intended to be limited to the embodiments shown herein but is to be accorded the widest scope consistent with the principles and novel features disclosed herein.