Comb tooth cutter clamp and method for machining comb tooth cutter by adopting same
Technical Field
The invention belongs to the technical field of cutter processing, and relates to a comb-tooth cutter clamp and a method for processing a comb-tooth cutter by using the same.
Background
The comb-tooth cutter is a cutter for processing straight teeth, helical teeth and herringbone gears according to the generating principle. The method is mainly used for processing the straight gear with less teeth, the helical gear, the herringbone gear, the duplicate gear with narrow clearance groove, the helical gear with the convex shoulder and the like, has the characteristics of low production cost and wide application range, and is suitable for processing single-piece small-batch products.
As shown in fig. 1 and 2, the comb blade has a rectangular blade body 1 and blade teeth 6 on the top of the blade body 1. For the convenience of positioning, the comb teeth knife is divided into six surfaces, namely a comb teeth knife wide surface 4 at the front side and the comb teeth knife wide surface 4 at the rear side, a comb teeth knife narrow surface 3 at the left side and the right side, a comb teeth knife bottom surface 5 and a comb teeth knife top surface. One of the comb-tooth cutter narrow faces 3 is used as a reference face 2 for measuring the cutter tooth base distance 8, and the consistency of the comb-tooth cutters is guaranteed. The tooth base distance 8 refers to the distance of the reference tooth 7 from the reference surface 2. The comb has a tip relief 9.
The existing processing technology of the comb-tooth cutter firstly forges materials into a rectangular cutter blank; then, carrying out primary treatment on six surfaces of the cutter blank, including milling and grinding; secondly, milling the tooth form of the comb-tooth cutter; and finally carrying out heat treatment. The steps are rough machining of the comb-tooth cutter. The fine machining of the comb blade obtained by the rough machining requires the following grinding steps: step 1, finely grinding two comb tooth cutter width surfaces 4; step 2, finely grinding the bottom surface 5 of the comb teeth cutter; step 3, finely grinding the rear angle of the comb teeth cutter; step 4, fine grinding the tooth form; and 5, grinding two comb-tooth-blade narrow surfaces 3, wherein one comb-tooth-blade narrow surface 3 is used as a reference surface 2. It should be noted that in steps 1, 2, and 3, the combing blade is processed on a common flat grinder. Since step 4 is to finish the tooth form, the comb tooth knife needs to be transferred to a numerical control flat grinder for processing. And 5, the comb teeth knife needs to be transferred to a common flat grinder again for processing. That is, from step 3 to step 4, and from step 4 to step 5, the comb teeth cutter needs to be turned over twice in the ordinary flat grinding and the numerical control flat grinding, and is clamped twice again, so that the preparation time of processing is undoubtedly increased, the process route is prolonged, and the production efficiency is reduced. However, because the comb teeth cutter has no special fixture, the clamping of the comb teeth cutter is mainly realized by a vice at present, and in order to enable the comb teeth cutters produced in the same batch to have the consistent cutter tooth base distance 8, the existing grinding process can be adopted even if the process route is unreasonable. In the existing process, although the consistency of the cutter tooth base distance 8 is expected to be obtained through the process route, in the actual operation process, the reference tolerance of the cutter tooth base distance 8 which is required finally is expected to be achieved through the ordinary flat grinding in the step 5, the reference tolerance is generally 0.01 mm-0.015 mm, the control is very difficult, and the out-of-tolerance is very easy.
In addition, the tooth base distance 8 is controlled by the final fine grinding of the comb-tooth cutter reference surface 2, and the vice can only clamp 1 comb-tooth cutter at one time. This causes a problem of a serious deterioration in processing efficiency.
Therefore, due to the lack of the special fixture, the current machining process cannot be optimized, the precision of the produced comb-tooth cutters in the same batch cannot guarantee the consistency, and the machining efficiency of the products and the machining precision of the batch products cannot meet the requirements.
Disclosure of Invention
In order to achieve the purpose, the invention provides a comb teeth cutter clamp and a method for machining a comb teeth cutter by adopting the clamp.
The technical scheme of the invention is as follows: the utility model provides a broach anchor clamps, includes base and draw-in groove, its characterized in that: the clamping groove is formed in the base, and a notch of the clamping groove is flush with the base; the clamping groove is a through groove body, one end of the clamping groove is open, and the other end of the clamping groove is provided with a baffle; a clamping part is arranged in the clamping groove, a cavity capable of clamping the cutter body of the comb-tooth cutter is reserved between the clamping part and the clamping groove, the side wall of the clamping groove and the clamping part are respectively attached to two wide surfaces of the comb-tooth cutter, the bottom of the clamping groove is attached to the bottom surface of the comb-tooth cutter, and the surface of the baffle is attached to the reference surface of the comb-tooth cutter; the base is provided with at least two clamping grooves which are arranged on the base at intervals in parallel, and the end parts of the adjacent clamping grooves are in the same plane.
Further, the cavity is provided with an inclination angle, the angle of the inclination angle is consistent with the tooth crest back angle of the comb teeth cutter, the cutter body of the comb teeth cutter is arranged in the cavity, and the back cutter face of the comb teeth cutter is positioned in the horizontal plane.
Furthermore, the clamping part is a pressing block, the length of the pressing block is consistent with that of the clamping groove, the pressing block is located on one side of the clamping groove, one side face of the pressing block is attached to the side wall of the clamping groove, the other side face of the pressing block is attached to the wide face of the comb-tooth cutter, and the pressing block is connected with the base in a locking mode through screws.
Furthermore, three screws which are positioned on a straight line and are at equal intervals are arranged on the pressing block and are in locking connection with the base.
Furthermore, the clamping part also comprises a backing plate, the backing plate is arranged between the pressing block and the comb-tooth cutter, and two side surfaces of the backing plate are respectively attached to the wide surfaces of the pressing block and the comb-tooth cutter.
Further, the tooth tip relief angle is 18 ° ± 5'.
A method for processing a comb-tooth cutter by adopting a comb-tooth cutter clamp comprises the following steps: forging a rectangular cutter blank, and milling and grinding the front, rear, left and right bottom surfaces of the cutter blank with allowance; milling a back angle and a tooth shape of the comb-tooth cutter, and reserving allowance to obtain a rough-machined comb-tooth cutter; carrying out heat treatment on the comb-tooth cutter; the method is characterized in that: and (3) carrying out finish machining on the comb-tooth cutter obtained by rough machining, wherein the finish machining comprises the following specific steps:
step 1, finely grinding two wide surfaces, two narrow surfaces, a bottom surface and a tooth top rear angle of the comb tooth cutter by a common flat grinding method; one narrow face of the comb tooth cutter is a reference face; obtaining a comb-tooth cutter with a reference surface;
step 2, stably clamping the broach cutter body obtained in the step 1 in a cavity of a broach cutter clamp, wherein a tooth-shaped part to be processed extends out of the upper part of a clamping groove; attaching the reference surface of the comb-tooth cutter to the plate surface of the baffle; finishing the clamping of the comb teeth cutter;
step 3, fixing the comb-tooth cutter clamp clamped in the step 2 on a machine tool, and finely grinding the tooth form of the comb-tooth cutter; obtaining the comb-tooth cutter with accurate cutter tooth base distance.
Further, after the clamping of the comb teeth cutter in the step 2 is finished, the tooth crest rear angle of the comb teeth cutter is in the horizontal plane.
Further, at least two identical comb blades obtained in the step 1 are clamped in the step 2.
Further, place the cutter body in the draw-in groove of broach anchor clamps in step 2, clamping part is the briquetting, and the briquetting is located one side of draw-in groove, and the briquetting passes through screw locking connection with the base, a side of briquetting and the lateral wall laminating of draw-in groove, another side with the laminating of the broadside of broach, the briquetting passes through screw and base locking connection, through the steadiness of backing plate adjustment centre gripping between the cutter body of briquetting and broach.
The invention has the beneficial effects that: due to the arrangement of the special fixture for the comb-tooth cutter, a plurality of identical comb-tooth cutters can be used for accurately processing the tooth form under the condition that the reference surface is kept consistent, and the consistency of the tooth base distances of the cutters is ensured. Not only improves the precision, but also improves the processing efficiency. Due to the assistance of the comb-tooth cutter clamp, the processing technology of the comb-tooth cutter is optimized, and after the finish grinding of each surface of the comb-tooth cutter is finished, the tooth profile is accurately processed on a machine tool through numerical control, so that multiple clamping and adjustment in the processing process are avoided, the consistency of the tooth profile and the consistency of the base distance of the cutter teeth are ensured, and the processing precision is ensured; and the processing route is shortened, and the processing efficiency is improved.
Drawings
Fig. 1 is a schematic structural view of the comb blade.
Fig. 2 is a left side view of fig. 1.
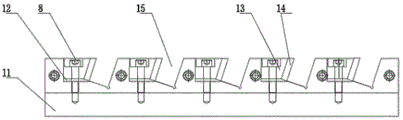
Fig. 3 is a schematic structural view of the comb blade holder.
Fig. 4 is a schematic structural view of the comb blade clamp clamping the comb blade.
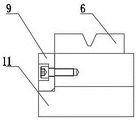
Fig. 5 is a left side view of fig. 4.
Fig. 6 is a top view of fig. 4.
In the figure: 1. the tool comprises a tool body, 2, a reference surface, 3, a narrow surface, 4, a wide surface, 5, a bottom surface, 6, tool teeth, 7, reference teeth, 8, screws, 9, a baffle, 10, a rear tool surface, 11, a base, 12, a clamping groove, 13, a pressing block, 14, a base plate, 15, a cavity, d tool tooth base distance and theta tooth crest relief angle.
Detailed Description
The technical solution in the embodiments of the present invention will be clearly and completely described below with reference to the accompanying drawings in the embodiments of the present invention.
As shown in fig. 3 to 6, a jig for a broach blade includes a base 11 and a catching groove 12. The card slot 12 is opened on the base 11. The notch of the card slot 12 is flush with the base 11. The slot 12 is a through slot on the base 11. One end of the clamping groove 12 is open, and the other end is provided with a baffle 9. The length of the clamping groove 12 can be used for stably clamping the comb-tooth cutter. A holding member is provided in the engaging groove 12. A cavity 15 capable of clamping the comb-tooth cutter body 1 is reserved between the clamping part and the clamping groove 12. The die cavity 15 and the cutter body are rectangular in shape. The clamping component can be a pressing block 13. The clamping member serves to firmly clamp the body 1 of the broach in the cavity 15. It should be noted that, in order to make the broach sword by firm centre gripping to guarantee follow-up profile of tooth precision processing. Therefore, after the clamping is completed, the clamping surface of the clamping component and the side wall of the clamping groove 12 are respectively in a state of being attached and abutted to the two wide surfaces 4 of the comb-tooth cutter and the bottom surface 5 of the clamping groove 12. Especially, the reference surface 2 of the comb-tooth cutter and the plate surface of the baffle 9 are ensured to be attached and abutted, and the flatness is less than 0.005 mm.
In order to increase the processing quantity of the same set of comb-teeth cutters, at least two clamping grooves 12 are arranged on the base 11. Five are preferred. Of course, the actual number of pockets 12 may be determined based on the length of the machine table. The plurality of card slots 12 are arranged in parallel at intervals. The requirement for this spacing is that adjacent comb blades cannot interfere after clamping is complete. The surfaces of the baffle plates 9 arranged at the end parts of the adjacent clamping grooves 12 are always in the same plane. This is to ensure that the same comb-teeth knife is clamped in different clamping grooves 12, and the reference surface 2 and the plate surface of the baffle 9 can be in the same plane. This is the guarantee to 8 consistencies of comb teeth sword base pitch.
Since the comb blade has a tip clearance angle 9, it is necessary that the flank 10 of the comb blade be machined in a horizontal plane in order to facilitate the milling of the tooth profile by the machine tool. One way is to tilt the entire clamp; another way is to incline the cavity 15 to have an inclination angle. The cavity 15 is preferably inclined in view of ease of operation and machining accuracy.
As an example, the cavity 15 is provided in an inclined configuration, and the holding member is defined as the compact 13. The invention is explained in further detail as follows:
the cavity 15 has an inclination angle which is in accordance with the tooth tip clearance angle 9 of the comb blade. The direction of inclination of the cavity 15 is determined according to the comb blade. When the cutter body 1 of the comb-tooth cutter is arranged in the cavity 15, the rear cutter face 10 of the comb-tooth cutter is in a horizontal plane.
When the cavity 15 has an inclination angle, one side of the pressing block 13 is a vertical surface and is attached to the side wall of the clamping groove 12; the inclined surface at the other side is attached to the wide surface 4 of the comb teeth cutter, and the inclined angle is the same as the angle of the tooth crest back angle 9. The length of the pressing block 13 is consistent with that of the clamping groove 12. The thickness of the pressing block 13 is smaller than the depth of the clamping groove 12. The pressing block 13 is provided with a vertical through hole, the base 11 is provided with a threaded hole at a corresponding position, and the pressing block 13 is in locking connection with the base 11 through a screw 8. In order to stably clamp the comb-tooth cutter, three vertical through holes are formed in the front, middle and rear parts of the pressing block 13, the three through holes are arranged at equal intervals, and the central points of the three through holes are located on a straight line. The base 11 is also provided with three threaded holes at corresponding positions. The pressing block 13 is connected with the base 11 in a locking way through three screws 8 passing through the base 11.
In order to adapt to comb blades of more specifications, the size of the cavity 15 between the clamping groove 12 and the clamping part needs to be adjustable. A backing plate 14 is provided for the clamping section to prevent it from becoming between the mass 13 and the comb blade. Two side surfaces of the backing plate 14 are respectively attached to the pressing block 13 and the wide surface 4 of the comb teeth cutter.
The comb-tooth cutter clamp provided by the invention can be suitable for comb-tooth cutters with 0-45-degree tooth crest back angles 9. A typical tip relief angle 9 is 18 ° ± 5'.
The following describes a method for machining a comb blade by using a comb blade fixture:
first, the comb blade is roughly machined.
Step a, blanking, namely forging the blank into a required cutter blank by adopting a high-speed steel material, and adding 4-5 mm of allowance for each length, width and height;
b, milling two wide surfaces 4, top surfaces and bottom surfaces 5 of the broach cutter, wherein the thickness allowance is 1.3-1.4 mm, and the height allowance is 1.3-1.4 mm;
c, grinding four surfaces of the comb teeth cutter in the step b, wherein the thickness allowance is 0.9-1.0 mm, and the height allowance is 0.9-1.0 mm;
d, vertically milling two narrow surfaces 3 of the comb tooth cutter, wherein the allowance is 0.5-0.6 mm;
step e, milling a tooth top rear angle 9, and reserving a blade zone of 0.5-1 mm close to the front surface;
step f, milling the tooth shape, wherein the tooth shape allowance is 0.45-0.6 mm;
step g, heat treatment, wherein the hardness of the heat treatment is 64-66 HRC.
Secondly, the rough machining comb teeth cutter is subjected to fine machining, and the rough machining comb teeth cutter is also a part of the key improvement of the invention.
Step 1, finely grinding two wide surfaces 4, two narrow surfaces 3, a bottom surface 5 and a tooth top back angle 9 of the comb teeth cutter by a common flat grinding method; one comb tooth cutter narrow face 3 is a reference face 2; this step results in a comb blade having a reference plane 2;
step 2, stably clamping the comb-tooth cutter body 1 obtained in the step 1 in a cavity 15 of a comb-tooth cutter clamp, wherein the tooth-shaped part to be processed extends out of the upper part of the clamping groove 12; attaching the reference surface 2 of the comb-tooth cutter to the plate surface of the baffle 9; finishing the clamping of the comb teeth cutter;
and 3, fixing the comb-tooth cutter clamp clamped in the step 2 on a machine tool, and finely grinding the tooth form of the comb-tooth cutter to obtain the comb-tooth cutter with the accurate cutter tooth base distance of 8.
After the clamping of the comb teeth cutter in the step 2 is finished, the tooth crest back angle 9 of the comb teeth cutter is in the horizontal plane. Therefore, the machine tool can more conveniently finish the tooth form.
In step 2, at least two identical comb blades obtained in step 1 are clamped. Therefore, the same batch of comb teeth cutters can be efficiently processed.
If the clamping component is the pressing block 13, in the step 2, the cutter body 1 of the comb-tooth cutter is placed on one side of the clamping groove 12, and the pressing block 13 is locked between the cutter body 1 and the other side of the clamping groove 12 through the screw 8. A backing plate 14 can be added between the pressing block 13 and the comb blade body 1 to adjust the clamping stability.
The comb-tooth cutter fixture can simultaneously clamp a plurality of identical comb-tooth cutter bodies 1, each cutter is independently installed, and the installation position can be flexibly adjusted, so that the machining efficiency of the comb-tooth cutter is improved in multiples. In addition, the same set of comb teeth cutter is clamped and processed at one time, the same cutter tooth base distance is 8, the reference consistency of the cutter is good, the consistency error reaches within 0.005mm, and the precision is stable.