CN112522867A - Automatic template assembly line - Google Patents
Automatic template assembly line Download PDFInfo
- Publication number
- CN112522867A CN112522867A CN202011425509.2A CN202011425509A CN112522867A CN 112522867 A CN112522867 A CN 112522867A CN 202011425509 A CN202011425509 A CN 202011425509A CN 112522867 A CN112522867 A CN 112522867A
- Authority
- CN
- China
- Prior art keywords
- boss
- pneumatic cylinder
- assembly
- fixed
- feeding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images

Classifications
-
- D—TEXTILES; PAPER
- D05—SEWING; EMBROIDERING; TUFTING
- D05B—SEWING
- D05B25/00—Sewing units consisting of combinations of several sewing machines
-
- D—TEXTILES; PAPER
- D05—SEWING; EMBROIDERING; TUFTING
- D05B—SEWING
- D05B35/00—Work-feeding or -handling elements not otherwise provided for
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Sewing Machines And Sewing (AREA)
Abstract
The invention provides an automatic template assembly line which comprises a transmission device, wherein the transmission device comprises a working platform, a first boss and a second boss are respectively arranged on two sides of the working platform, transmission belts are respectively arranged on the first boss and the second boss, three material pushing assemblies are arranged on the side wall of the first boss, a cache device is arranged on one side of each material pushing assembly, each cache device comprises a cache box, a material feeding assembly is arranged on the side wall of each cache box, a lifting assembly is arranged in each cache box, a processing device is arranged on one side of each cache box, each processing device comprises a processing platform, a sewing machine is arranged on one side of each processing platform, a base frame is fixed on each processing platform, a through hole is formed in each base frame, a sliding block is connected to each base frame in a sliding mode, a driving assembly is arranged. The invention relates to an automatic template assembly line which can store templates, is convenient for uninterrupted operation of a sewing machine and is convenient for loading and unloading the templates.
Description
Technical Field
The invention mainly relates to the technical field of sewing equipment, in particular to an automatic template assembly line.
Background
The automatic template assembly line can sew the fabric fixed on the template.
According to the template sewing production line provided by the patent document with the application number of CN201920614653.7, the product comprises a template and a plurality of template sewing machines, wherein the template sewing machines are connected through a conveyor; the template sewing machine comprises a machine head, a workbench, an electric two-axis linear module and a template clamp; the template clamp comprises a bracket and two groups of locking mechanisms, wherein each locking mechanism comprises a rotating shaft, a cam, a first pull rod, a second pull rod, a coil spring and a rotating shaft driving device; the cam is fixedly connected with the rotating shaft; the first pull rod is rotatably connected with the rotating shaft, and the coil spring is arranged between the first pull rod and the rotating shaft; the bracket is provided with a limit pin; the cam and the first pull rod rotate relatively to drive the second pull rod to slide relative to the first pull rod; lock pins are arranged on two sides of the template, and lock hooks matched with the lock pins are arranged at the end parts of the second pull rods; and the support is provided with a positioning plate matched with the end face of the template. The product can reduce the error rate and ensure the sewing precision.
The product in the above-mentioned patent can reduce the error rate, guarantees the sewing precision, nevertheless has the template quantity too much to store up the possibility that influences the assembly line work on the assembly line, consequently needs to design one kind and can save the template, the sewing machine uninterrupted duty of being convenient for, the automatic template assembly line of being convenient for template packing into and unloading out.
Disclosure of Invention
The invention mainly provides an automatic template production line, which is used for solving the technical problems in the background technology.
The technical scheme adopted by the invention for solving the technical problems is as follows:
an automatic template assembly line comprises a transmission device, wherein the transmission device comprises a working platform, a first boss and a second boss are respectively arranged on two sides of the working platform, transmission belts are respectively arranged on the first boss and the second boss, three material pushing assemblies are arranged on the side wall of the first boss in an equidistant manner, a buffer device is arranged on one side of each material pushing assembly, the buffer device comprises a buffer box, the buffer box is fixed on the side wall of the first boss, a material feeding assembly is arranged on the side wall of the buffer box, a lifting assembly is arranged in the buffer box, a processing device is arranged on one side of each buffer box, the processing device comprises a processing platform, two ends of the processing platform are respectively connected with the side wall of the first boss and the side wall of the second boss, a sewing machine is arranged on one side of the processing platform, a base frame is fixed on the processing platform, and a through hole is arranged, the base frame is connected with a sliding block in a sliding mode, a driving assembly is arranged on one side of the sliding block, and a positioning assembly is arranged at the bottom of the sliding block.
Preferably, the material pushing assembly comprises a material pushing pneumatic cylinder, the material pushing pneumatic cylinder is fixed on the first boss side wall, and the output end of the material pushing pneumatic cylinder penetrates through the first boss side wall to be connected with the pushing block. In the preferred embodiment, the template is pushed into the caching device conveniently through the pushing assembly.
Preferably, the material loading subassembly includes flitch and material loading pneumatic cylinder, the flitch runs through the buffer memory case lateral wall and extends to inside, material loading pneumatic cylinder is fixed at the buffer memory case lateral wall, material loading pneumatic cylinder output connects the flitch lateral wall. In the preferred embodiment, the feeding assembly is convenient for feeding the templates in the cache box one by one.
Preferably, the lifting assembly comprises a lifting pneumatic cylinder, the lifting pneumatic cylinder is fixed at the bottom of the inner wall of the buffer box, and the output end of the lifting pneumatic cylinder is connected with the base plate. In the preferred embodiment, the stable movement of the forms into the cache box is facilitated by the lift assembly.
Preferably, the buffer box is far away from one side of the feeding assembly is provided with a feeding hole, one side of the feeding hole is provided with a limiting block, and the limiting block is fixed on the processing platform. In the preferred embodiment, the positioning of the template after feeding is facilitated through the limiting block.
Preferably, the driving assembly comprises a fixing box, the fixing box is fixed on the base frame, a driving motor is fixed in the fixing box, the output end of the driving motor is connected with a screw rod, the screw rod is connected with a sliding block through a screw nut, and a bearing at the other end of the screw rod is connected with the base frame. In the preferred embodiment, the driving force is provided for the sliding of the slider by the driving assembly.
Preferably, the locating component includes flexible pneumatic cylinder, flexible pneumatic cylinder runs through-hole link block, shell case is connected to flexible pneumatic cylinder output, shell incasement fixed drive motor, the drive motor output runs through shell case and connects elasticity subassembly. In the preferred embodiment, the elastic component is lifted and lowered conveniently by the telescopic pneumatic cylinder, and is rotated conveniently by the transmission motor.
Preferably, the elasticity subassembly includes fixed disk and connecting rod, the transmission motor output is connected to the fixed disk, two the connecting rod all runs through the fixed disk and connects the pressure disk, two the spring is all established to the connecting rod outer wall cover. In the preferred embodiment, the stable compression of the movable platen is facilitated by the resilient member.
Compared with the prior art, the invention has the beneficial effects that:
according to the template conveying device, templates are conveniently conveyed through the conveying belt, the templates are conveniently and stably moved into the buffer box through the lifting assembly, the templates on the conveying belt are conveniently buffered through the buffer device, the pressure of the conveying belt is reduced, the efficient work of the sewing machine is guaranteed, the templates are conveniently and stably moved into the buffer box through the lifting assembly in the buffer device, the templates in the buffer box are conveniently fed one by one through the feeding assembly, the templates are conveniently positioned after being fed through the limiting blocks, the fabrics in the templates are conveniently processed through the processing device, the fabrics in the templates are sewn through the sewing machine in the processing device, the elastic assembly is conveniently lifted through the telescopic pneumatic cylinder, the elastic assembly is conveniently rotated through the transmission motor, the elastic assembly is convenient for stably pressing the movable templates, the driving assembly provides driving force for sliding of the sliding block, and the sliding block drives the templates to.
The present invention will be explained in detail below with reference to the drawings and specific embodiments.
Drawings
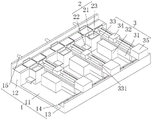
FIG. 1 is an isometric view of the overall construction of the present invention;
FIG. 2 is an isometric view of the positioning assembly structure of the present invention;
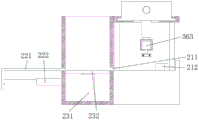
FIG. 3 is a side view of the structure of the buffer device of the present invention;
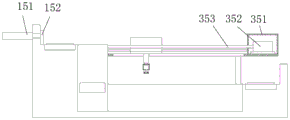
fig. 4 is a side view of the overall structure of the present invention.
In the figure: 1. a transmission device; 11. a working platform; 12. a first boss; 13. a second boss; 14. a conveyor belt; 15. a material pushing assembly; 151. a material pushing pneumatic cylinder; 152. a push block; 2. a cache device; 21. a cache box; 211. a feeding port; 212. a limiting block; 22. a feeding assembly; 221. feeding plates; 222. a feeding pneumatic cylinder; 23. a lifting assembly; 231. a lifting pneumatic cylinder; 232. a base plate; 3. a processing device; 31. a processing platform; 32. a sewing machine; 33. a base frame; 331. a through hole; 34. a slider; 35. a drive assembly; 351. a fixed box; 352. a drive motor; 353. a screw rod; 36. a positioning assembly; 361. a telescopic pneumatic cylinder; 362. a housing case; 363. a drive motor; 364. an elastic component; 3641. fixing the disc; 3642. a connecting rod; 3643. a platen; 3644. a spring.
Detailed Description
In order to facilitate an understanding of the invention, the invention will now be described more fully hereinafter with reference to the accompanying drawings, in which several embodiments of the invention are shown, but which may be embodied in different forms and not limited to the embodiments described herein, but which are provided so as to provide a more thorough and complete disclosure of the invention.
It will be understood that when an element is referred to as being "secured to" another element, it can be directly on the other element or intervening elements may be present, and when an element is referred to as being "connected" to another element, it can be directly connected to the other element or intervening elements may also be present, as the terms "vertical", "horizontal", "left", "right" and the like are used herein for descriptive purposes only.
Unless defined otherwise, all technical and scientific terms used herein have the same meaning as commonly understood by one of ordinary skill in the art to which this invention belongs, and the knowledge of the terms used herein in the specification of the present invention is for the purpose of describing particular embodiments and is not intended to limit the present invention, and the term "and/or" as used herein includes any and all combinations of one or more of the associated listed items.
Please refer to fig. 1 and 4 again, an automatic template assembly line includes a transmission device 1, the transmission device 1 includes a working platform 11, two sides of the working platform 11 are respectively provided with a first boss 12 and a second boss 13, the first boss 12 and the second boss 13 are both provided with a transmission belt 14, the side wall of the first boss 12 is provided with three pushing assemblies 15 with equal distance, the pushing assemblies 15 include a pushing pneumatic cylinder 151, the pushing pneumatic cylinder 151 is fixed on the side wall of the first boss 12, and the output end of the pushing pneumatic cylinder 151 penetrates through the side wall of the first boss 12 to connect with a pushing block 152. The template to be sewn is continuously put on the transmission belt 14 on the first boss 12 by the worker, the template is transported on the transmission belt 14, and when the template is transported to the material pushing assembly 15, the template is pushed into the buffer box 21 by the material pushing pneumatic cylinder 151.
Please refer to fig. 1 and 3, a buffer device 2 is disposed on one side of each pushing assembly 15, the buffer device 2 includes a buffer box 21, the buffer box 21 is fixed on the sidewall of the first boss 12, a feeding assembly 22 is disposed on the sidewall of the buffer box 21, a lifting assembly 23 is disposed in the buffer box 21, the feeding assembly 22 includes a feeding plate 221 and a feeding pneumatic cylinder 222, the feeding plate 221 extends through the sidewall of the buffer box 21 to the inside, the feeding pneumatic cylinder 222 is fixed on the sidewall of the buffer box 21, the output end of the feeding pneumatic cylinder 222 is connected to the sidewall of the feeding plate 221, the lifting assembly 23 includes a lifting pneumatic cylinder 231, the lifting pneumatic cylinder 231 is fixed at the bottom of the inner wall of the buffer box 21, the output end of the lifting pneumatic cylinder 231 is connected to a backing plate 232, a feeding port 211 is disposed on the side of the buffer box 21 away from the feeding assembly 22, and a limit block 212 is disposed on the side of the feeding, the limiting block 212 is fixed on the processing platform 31. The plurality of buffer devices 2 can uniformly receive the processing-substituted templates, the templates fall on the base plate 232 when entering the buffer box 21, the lifting pneumatic cylinder 231 can drive the base plate 232 to move, the base plate 232 continuously moves downwards along with the continuous entering of the templates, the output end of the lifting pneumatic cylinder 231 needs to retract to the bottom firstly during feeding, the output end of the feeding pneumatic cylinder 222 drives the feeding plate 221 to move, the templates on the base plate 232 are pushed out through the feeding port 211, and the templates are pushed out to the template attaching limit block 212.
Please refer to fig. 1-4, a processing device 3 is disposed on one side of each buffer box 21, the processing device 3 includes a processing platform 31, two ends of the processing platform 31 are respectively connected to the side walls of the first boss 12 and the second boss 13, a sewing machine 32 is disposed on one side of the processing platform 31, a base frame 33 is fixed on the processing platform 31, a through hole 331 is disposed on the base frame 33, a slide block 34 is slidably connected on the base frame 33, a driving component 35 is disposed on one side of the slide block 34, a positioning component 36 is disposed at the bottom of the slide block 34, the driving component 35 includes a fixing box 351, the fixing box 351 is fixed on the base frame 33, a driving motor 352 is fixed in the fixing box 351, an output end of the driving motor 352 is connected to a lead screw 353, the lead screw 353 is connected to the lead screw nut and the slide block 34, the other end of the, locating component 36 includes flexible pneumatic cylinder 361, flexible pneumatic cylinder 361 runs through-hole 331 link block 34, shell case 362 is connected to flexible pneumatic cylinder 361 output, shell case 362 internal fixation drive motor 363, drive motor 363 output runs through shell case 362 and connects elasticity subassembly 364, elasticity subassembly 364 includes fixed disk 3641 and connecting rod 3642, the output of drive motor 363 is connected to fixed disk 3641, two connecting rod 3642 all runs through fixed disk 3641 and connects pressure disk 3643, two spring 3644 is all established to the cover of connecting rod 3642 outer wall. When in processing, the telescopic pneumatic cylinder 361 drives the fixed disc 3641 to move downwards, a pressure disc 3643 at the bottom of the fixed disc 3641 compresses the upper surface of the template, the driving motor 352 is started, the output end of the driving motor 352 drives the screw rod 353 to rotate, the screw rod 353 rotates to drive the slider 34 to move, the slider 34 drives the template to move, the sewing machine 32 performs sewing when the template is moved to the sewing machine 32, the driving motor 352 can also be started, the output end of the driving motor 352 can drive the template to rotate on the processing platform 31, the sewing of the sewing machine 32 is facilitated, the template is moved into the transmission belt 14 on the second boss 13 through the slider 34 in a sliding mode.
The specific operation mode of the invention is as follows:
a worker continuously puts a template to be sewn on a transmission belt 14 on a first boss 12, the template is transported on the transmission belt 14, when the template is transported to a material pushing assembly 15, a material pushing pneumatic cylinder 151 pushes the template into a buffer box 21, a plurality of buffer devices 2 can uniformly receive a substitute processing template, the template falls on a base plate 232 firstly when entering the buffer box 21, a lifting pneumatic cylinder 231 can drive the base plate 232 to move, the base plate 232 continuously moves downwards along with the continuous entering of the template, when the template is fed, the output end of the lifting pneumatic cylinder 231 retracts to the bottommost part, then the output end of a feeding pneumatic cylinder 222 drives a feeding plate 221 to move, the template on the base plate 232 is pushed out through a feeding port 211 and is pushed out to a template close limiting block 212, when the telescopic pneumatic cylinder 361 drives a fixed plate 3641 to move downwards, a pressure plate 3643 at the bottom of the 3641 tightly presses the upper surface of the template, at the moment, a driving motor 352, the screw 353 rotates to drive the slider 34 to move, the slider 34 drives the template to move, the sewing machine 32 performs sewing when the template is moved to the sewing machine 32, the driving motor 352 can be started, the output end of the driving motor 352 can drive the template to rotate on the processing platform 31, sewing of the sewing machine 32 is facilitated, the template is moved into the transmission belt 14 on the second boss 13 through sliding of the slider 34 after sewing is completed, and discharging is completed.
The invention is described above with reference to the accompanying drawings, it is obvious that the invention is not limited to the above-described embodiments, and it is within the scope of the invention to adopt such insubstantial modifications of the inventive method concept and solution, or to apply the inventive concept and solution directly to other applications without modification.
Claims (8)
1. The automatic template production line comprises a transmission device (1) and is characterized in that the transmission device (1) comprises a working platform (11), wherein a first boss (12) and a second boss (13) are respectively arranged on two sides of the working platform (11), transmission belts (14) are respectively arranged on the first boss (12) and the second boss (13), three material pushing assemblies (15) are arranged on the side wall of the first boss (12) in an equidistance mode, a buffer device (2) is arranged on one side of each material pushing assembly (15), each buffer device (2) comprises a buffer box (21), each buffer box (21) is fixed on the side wall of the first boss (12), a feeding assembly (22) is arranged on the side wall of each buffer box (21), a lifting assembly (23) is arranged in each buffer box (21), and a processing device (3) is arranged on one side of each buffer box (21), processingequipment (3) are including processing platform (31), first boss (12) and second boss (13) lateral wall are connected respectively at processing platform (31) both ends, processing platform (31) one side is equipped with sewing machine (32), fixed base frame (33) on processing platform (31), be equipped with through-hole (331) on base frame (33), sliding connection slider (34) on base frame (33), slider (34) one side is equipped with drive assembly (35), slider (34) bottom is equipped with locating component (36).
2. The automatic template production line according to claim 1, wherein the pushing assembly (15) comprises a pushing pneumatic cylinder (151), the pushing pneumatic cylinder (151) is fixed on the side wall of the first boss (12), and the output end of the pushing pneumatic cylinder (151) penetrates through the side wall of the first boss (12) to be connected with the pushing block (152).
3. The automatic stencil production line of claim 1, wherein the feeding assembly (22) comprises a feeding plate (221) and a feeding pneumatic cylinder (222), the feeding plate (221) extends through the sidewall of the buffer box (21) to the inside, the feeding pneumatic cylinder (222) is fixed on the sidewall of the buffer box (21), and the output end of the feeding pneumatic cylinder (222) is connected to the sidewall of the feeding plate (221).
4. The automatic template assembly line according to claim 1, wherein the lifting assembly (23) comprises a lifting pneumatic cylinder (231), the lifting pneumatic cylinder (231) is fixed at the bottom of the inner wall of the buffer box (21), and the output end of the lifting pneumatic cylinder (231) is connected with a backing plate (232).
5. The automatic template production line according to claim 1, wherein a feeding opening (211) is formed in one side, away from the feeding assembly (22), of the buffer box (21), a limiting block (212) is arranged on one side of the feeding opening (211), and the limiting block (212) is fixed on the processing platform (31).
6. The automated stencil production line of claim 1, wherein the driving assembly (35) comprises a fixing box (351), the fixing box (351) is fixed on the base frame (33), a driving motor (352) is fixed in the fixing box (351), an output end of the driving motor (352) is connected with a screw rod (353), the screw rod (353) is connected with a screw nut connecting slide block (34), and the other end of the screw rod (353) is connected with the base frame (33) in a bearing way.
7. The automatic template production line of claim 1, wherein the positioning assembly (36) comprises a telescopic pneumatic cylinder (361), the telescopic pneumatic cylinder (361) penetrates through a through hole (331) to be connected with the sliding block (34), the output end of the telescopic pneumatic cylinder (361) is connected with a housing box (362), a transmission motor (363) is fixed in the housing box (362), and the output end of the transmission motor (363) penetrates through the housing box (362) to be connected with an elastic assembly (364).
8. The automatic template production line according to claim 7, wherein the elastic component (364) comprises a fixed disc (3641) and connecting rods (3642), the fixed disc (3641) is connected with the output end of the transmission motor (363), the two connecting rods (3642) penetrate through the fixed disc (3641) and are connected with a pressure plate (3643), and springs (3644) are sleeved on the outer walls of the two connecting rods (3642).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011425509.2A CN112522867A (en) | 2020-12-09 | 2020-12-09 | Automatic template assembly line |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011425509.2A CN112522867A (en) | 2020-12-09 | 2020-12-09 | Automatic template assembly line |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN112522867A true CN112522867A (en) | 2021-03-19 |
Family
ID=74996739
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202011425509.2A Pending CN112522867A (en) | 2020-12-09 | 2020-12-09 | Automatic template assembly line |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN112522867A (en) |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB958670A (en) * | 1960-09-01 | 1964-05-21 | Wallwin Turning Machines Ltd | Mechanism for template stitching |
| CN205346261U (en) * | 2015-12-29 | 2016-06-29 | 福建泉工股份有限公司 | Layer board memory device |
| CN107235320A (en) * | 2017-06-28 | 2017-10-10 | 江苏哈工药机科技股份有限公司 | A kind of corner brace automatic charging machine people |
| CN208649610U (en) * | 2018-05-31 | 2019-03-26 | 温州忆捷科技有限公司 | A kind of pkt. flap sewing device |
| CN110485063A (en) * | 2019-08-21 | 2019-11-22 | 宁波易高智能装备有限公司 | A kind of press equipment of diversification periphery sewing |
| WO2020024808A1 (en) * | 2018-08-03 | 2020-02-06 | 山东舒朗电子商务有限公司 | Integral sewing template and method for knitting slit, forming swing angle, and sewing up |
| CN210595070U (en) * | 2019-07-17 | 2020-05-22 | 宜兴市永优五金机械有限公司 | Automatic feeding device for folding rod of trolley |
| JP2020122723A (en) * | 2019-01-31 | 2020-08-13 | 株式会社タカトリ | Contour recognition device for workpiece, sewing device, and method therefore |
| CN212051856U (en) * | 2020-01-17 | 2020-12-01 | 温州忆捷科技有限公司 | Template positioning mechanism of sewing machine |
| CN214458694U (en) * | 2020-12-09 | 2021-10-22 | 申洲针织(安徽)有限公司 | Automatic template assembly line |
-
2020
- 2020-12-09 CN CN202011425509.2A patent/CN112522867A/en active Pending
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB958670A (en) * | 1960-09-01 | 1964-05-21 | Wallwin Turning Machines Ltd | Mechanism for template stitching |
| CN205346261U (en) * | 2015-12-29 | 2016-06-29 | 福建泉工股份有限公司 | Layer board memory device |
| CN107235320A (en) * | 2017-06-28 | 2017-10-10 | 江苏哈工药机科技股份有限公司 | A kind of corner brace automatic charging machine people |
| CN208649610U (en) * | 2018-05-31 | 2019-03-26 | 温州忆捷科技有限公司 | A kind of pkt. flap sewing device |
| WO2020024808A1 (en) * | 2018-08-03 | 2020-02-06 | 山东舒朗电子商务有限公司 | Integral sewing template and method for knitting slit, forming swing angle, and sewing up |
| JP2020122723A (en) * | 2019-01-31 | 2020-08-13 | 株式会社タカトリ | Contour recognition device for workpiece, sewing device, and method therefore |
| CN210595070U (en) * | 2019-07-17 | 2020-05-22 | 宜兴市永优五金机械有限公司 | Automatic feeding device for folding rod of trolley |
| CN110485063A (en) * | 2019-08-21 | 2019-11-22 | 宁波易高智能装备有限公司 | A kind of press equipment of diversification periphery sewing |
| CN212051856U (en) * | 2020-01-17 | 2020-12-01 | 温州忆捷科技有限公司 | Template positioning mechanism of sewing machine |
| CN214458694U (en) * | 2020-12-09 | 2021-10-22 | 申洲针织(安徽)有限公司 | Automatic template assembly line |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US7018194B2 (en) | Powder supplying apparatus and powder molding apparatus | |
| CN207444403U (en) | A kind of automatic severing blanking machine of gum shoes surfacing material | |
| CN109531125B (en) | A three-dimensional automatic screw locking machine | |
| CN114378571B (en) | Automatic hinge assembly machine | |
| CN113579689A (en) | Cylindrical bearing assembly equipment for intelligent manufacturing | |
| CN208738035U (en) | Kinking foot machine | |
| CN114346675B (en) | Automatic hinge assembly machine | |
| CN214458694U (en) | Automatic template assembly line | |
| CN204906866U (en) | A automatic clicker for making flexible circuit board | |
| CN112079106B (en) | Transfer mechanism of operation device and operation classification equipment using same | |
| CN212371233U (en) | Material circulation device, drilling mechanism and machining center | |
| CN114655742B (en) | A crumpled bag printing feeding mechanism and feeding method capable of fast loading and unloading | |
| CN220323477U (en) | Tool for chip test | |
| CN222450659U (en) | Automatic punching equipment | |
| CN209477670U (en) | A three-dimensional automatic locking screw machine | |
| CN217707523U (en) | Adjustable conveyer belt mechanism | |
| CN213210418U (en) | Double-station double-hole testing machine for flexible cable | |
| CN112959063A (en) | Mobile phone assembly production line jig and workpiece auxiliary carrying device | |
| KR100297392B1 (en) | device for cenyering burn-in board in sorting handler for bum-in tester | |
| CN112808898B (en) | Full-automatic IC pin integer equipment | |
| CN209814374U (en) | Electronic components carrier band packaging mechanism | |
| CN223644191U (en) | A fan cover injection molding robot | |
| CN109159239B (en) | A bed board automatic claw nail machine | |
| CN218931192U (en) | Material strip feeding equipment capable of preventing material returning | |
| CN113247681A (en) | Stacking jacking device, stacking equipment and method |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WD01 | Invention patent application deemed withdrawn after publication | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20210319 |