High-efficiency energy-saving environment-friendly gas/oil steam boiler
Technical Field
The invention relates to the technical field of boilers, in particular to a high-efficiency energy-saving environment-friendly gas/oil steam boiler.
Background
With the rapid development of social economy, boilers are widely used in modern industry, electric power and people's life as process equipment for producing heat energy and power, and gas boilers meet the requirements of people on environment, safety and automation by virtue of the characteristics of high quality, environmental protection and cleanness, so that the gas boilers are adopted as heating equipment in many projects.
The gas boiler comprises two systems of gas combustion equipment and a boiler body. The gas combustion equipment mainly refers to a hearth and a combustor and also comprises other equipment related to the combustion process, and the gas combustion equipment mainly has the main function that a certain amount of combustible gas and air are introduced into the combustion equipment, and chemical energy is converted into heat energy through the combustion of the combustible gas, so that continuous heat energy is provided for a boiler body. The boiler body converts water into steam by means of heat energy provided by combustion equipment, so that the steam becomes a certain amount and quality (pressure and humidity). The whole boiler production process is that a certain amount of combustible gas and a corresponding amount of air are fed into the boiler for combustion, and the heat generated by combustion is transferred to water, so that the water is vaporized under a constant pressure to form water vapor with a certain pressure and temperature.
In many boilers, the equipment of the steam boiler is simple and compact in structure, and the pollution of the combustion products to the atmosphere is small, but the steam boiler has the defects that the fuel is mostly flammable and combustible gas, so that the safety requirement on the equipment of the boiler is very high. However, the existing boiler has some problems in the use process: due to various reasons, the explosion accidents of the gas-fired boiler frequently occur, which not only causes a great amount of economic loss, but also seriously threatens people in mind, body and even life.
The operation of the boiler should follow the principle of 'high efficiency and environmental protection', namely, the high efficiency utilization of fuel is ensured and the discharge amount of harmful substances NO and CO is reduced. Firstly, to ensure the sufficient combustion of the fuel, there are many factors that affect the combustion efficiency of the fuel, such as the area of the fuel inlet, the air intake speed, the air excess coefficient, etc. The inlet area and the wind speed of the fuel influence the flow field in the hearth, and the air inlet flow of the fuel is required to cause the disturbance in the hearth, so that the heat generated by combustion can be ensured to flow in the hearth, but a large amount of vortex bodies cannot exist in the hearth, and the stability of combustion reaction can be influenced. The air excess factor is required to satisfy the requirement of O for combustion reaction2In addition, the heat loss caused by smoke discharge should be reduced.
The boiler can consume a large amount of fuel in the production process, simultaneously produces along with a large amount of flue gases, because the exhaust gas temperature of general boiler is all very high, and has certain requirement to the temperature in the boiler furnace hall, so all need retrieve the flue gas waste heat. At present, the flue gas waste heat recovery of most boilers mainly adopts a mode of generating steam by using a waste heat boiler, but for most enterprises, the steam generated by the waste heat boiler is surplus, particularly in summer, the phenomenon of steam evacuation often occurs, and meanwhile, because the waste heat boiler of the enterprise is serious in aging, most of steam generation efficiency is lower, the energy system matching of the enterprise is unreasonable, and the problem of serious waste heat resource waste exists. In actual production, the waste heat recovery has certain difficulty because if the exhaust gas temperature is low, the conventional heat exchanger is adopted, the heat transfer temperature difference between the flue gas and the working medium in the heating surface at the tail part of the boiler is reduced, the heat transfer area is increased, and a plurality of pipes are densely arranged in a limited space, so that the flow resistance of the flue gas is increased, the power consumption of wind pressure is increased, and the metal consumption and the initial investment of equipment are increased.
Disclosure of Invention
Aiming at the technical problems of low boiler safety, insufficient fuel combustion and high waste heat recovery difficulty in the prior art, the invention aims to provide the efficient energy-saving environment-friendly gas/oil steam boiler which is high in safety, can fully combust fuel and can effectively recover waste heat.
The high-efficiency energy-saving environment-friendly gas/oil steam boiler comprises a boiler body, wherein the boiler body comprises a hearth, a heat exchange unit, a steam drum and a boiler wall; the heat exchange unit comprises a water-cooled wall, a first heat exchange tube and a second heat exchange tube, the water-cooled wall is longitudinally arranged to divide the hearth into a combustion area and a convection area, and the combustion area and the convection area form a loop channel; the first heat exchange tubes are vertically arranged along the interfaces of two sides of the combustion zone and the interface of the convection zone, and the water-cooled wall is connected with the first heat exchange tubes in the corresponding areas into a whole; the second heat exchange tube is vertically arranged in the convection zone; the lower ends of the first heat exchange tube and the second heat exchange tube are converged to a longitudinal lower collecting tube, and the upper ends of the first heat exchange tube and the second heat exchange tube are converged to a longitudinal upper collecting tube; the steam pocket is arranged outside the hearth and communicated with the upper part of the upper collecting pipe; the furnace wall is coated outside the hearth and the steam drum.
Preferably, the boiler body further comprises a waste heat utilization system, the waste heat utilization system comprises an energy saver, a circulating water pump and a heat preservation water tank, the lower end of the energy saver is located at the tail end of the hearth and is communicated with an outlet of the convection zone, a multi-loop pipeline is arranged in the energy saver, and a flue gas outlet is formed in the upper end of the energy saver; the multi-loop pipeline is designed by adopting an S-shaped loop curved surface structure, the heat-preservation water tank and the multi-loop pipeline form a water circulation system through a water pipe and provide circulating power by the circulating water pump, and water enters from the upper end of the multi-loop pipeline and exits from the lower end of the multi-loop pipeline; the heat preservation water tank is communicated with the lower collecting pipe through a water pipe and a boiler feed pump to supply water.
Preferably, the second heat exchange tube and the multi-loop pipeline are finned tubes; the lower half part of the multi-loop pipeline is a pressure-bearing section, the upper half part of the multi-loop pipeline is a normal-pressure section, the wall of the pressure-bearing section is thicker than that of the normal-pressure section, and the inner diameter of the pressure-bearing section is smaller than that of the normal-pressure section.
Preferably, the convection zone is divided into two opposite flow channels, wherein two rows of the second heat exchange tubes are arranged in the flow channel adjacent to the combustion zone, and one row of the second heat exchange tubes is arranged in the other flow channel.
Preferably, the hearth is provided with an explosion-proof device, and the explosion-proof device comprises a door body, a cover plate and an elastic resetting piece; the door body is fixed on the opening of the hearth through bolts and is provided with an air release hole; elasticity resets and includes spring and spring holder, the spring holder is fixed on the door body, the spring mounting in the spring holder and the outer end with the cover connection, the spring will the apron is taut to be made the apron lid is in on the door body and will the hole of disappointing plugs up.
Preferably, the energy-efficient and environment-friendly gas/oil steam boiler of the present invention further comprises a burner for feeding fuel and oxygen into the combustion zone.
The burner plays a decisive role in the combustion state of the boiler, so that certain requirements are imposed on the technology of the burner, and the burner is required to reach rated power under certain conditions. The burner type is matched to the furnace size in order to create the best combustion conditions for the flame inside the furnace. The device also can be flexibly adjusted, and can be operated at high load and low load; at the same time, the emission of harmful gases in the hearth is required to be minimized.
In the automatic boiler control system, the important part is to regulate and control the fuel flow and the air flow according to a certain proportional relation, and because the feedback mechanisms of a fuel quantity control loop and an air quantity control loop are different, once the boiler load changes, the change of the air flow is slower than that of the fuel quantity. The measurement modes are different, and because the boiler fuel sources comprise coke oven gas and blast furnace gas, the supply and the ratio of the fuel are unstable, and the burner has certain change, so that the fixed ratio is difficult to ensure. Especially when the load of the boiler fluctuates rapidly, the air quantity and the fuel quantity can not be ensured to be in proper proportion. Because of the need to solve the above regulation problem, ensuring that the boiler control system is in the optimum state, an optimized analysis of the boiler combustion scheme is required.
Preferably, the combustor is equipped with a multivariable-based PID proportional control system. The air, pressure (fuel quantity) and water supply quantity can be accurately controlled in a proportion loop manner, so that the hearth achieves the most efficient combustion effect, high-temperature flue gas passes through the energy saver and the flue gas heat recovery system, is subjected to tail gas purification treatment and then is discharged up to the standard, and the heat efficiency is more than or equal to 93%.
Preferably, the steam drum can be provided with a pressure gauge, a pressure transmitter and a pressure controller; thermometers can be arranged in the steam drum and the hearth; the steam pocket is provided with a main steam pipe and a safety valve.
Preferably, the water level monitoring and early warning device is used for monitoring the water level of the boiler.
Preferably, the water level monitoring and early warning device comprises a communicating pipe and a magnetic turning plate liquid level meter, the upper end of the communicating pipe is communicated with the steam drum, the lower end of the communicating pipe is communicated with the lower collecting pipe, and the magnetic turning plate liquid level meter is arranged on the communicating pipe and is close to the upper collecting pipe in height.
Preferably, a magnetic flap level meter and a prompting device can be arranged in the heat-preservation water tank and used for monitoring the water level in the heat-preservation water tank and avoiding the water in the heat-preservation water tank from being used up.
Preferably, the efficient energy-saving environment-friendly gas/oil steam boiler further comprises a steel frame outer package, and the boiler body is wrapped by the steel frame outer package.
The test parameters of the instrument can be used as the parameter basis of a multivariable PID proportional control system to realize the intelligent control of the boiler.
The key technology and positive progress effect of the invention are as follows:
1. multi-stage heat exchange design and waste heat utilization system design
In the boiler body, a hearth is divided into a combustion area and a convection area, fuel and oxygen can be combusted in the combustion area, a water cooling wall and a first heat transfer pipe are heated by radiation heat transfer, then fuel gas enters the convection area and is heated by convection heat transfer to a second heat transfer pipe, the water cooling wall and the first heat transfer pipe at an interface, multi-stage heat exchange is carried out in the hearth, heat is efficiently transferred to water in the heat exchange pipes, and the energy conversion efficiency of the hearth is effectively improved; the waste heat utilization system is arranged close to the boiler body and comprises a multi-loop pipeline type energy saver, a water circulation system and the like, the waste heat multi-loop pipeline is designed by adopting an S-shaped loop curved surface structure, the heat contact area is increased, dust is not easy to attach, the maximum heat recovery is realized, the process water is preheated by utilizing the water circulation system, the heat efficiency is further improved, and the purposes of energy conservation and emission reduction are achieved.
The combustion zone, the convection zone and the energy saver can carry out multi-stage heat exchange, not only can strengthen heat exchange, but also is more beneficial to steam pressure adjustment through the adjustment of the front water volume and the back water volume, can avoid bursting risk caused by severe change of steam pressure, improves the safety performance of the boiler, and can meet the technical requirements of a D-grade boiler (the steam pressure is less than or equal to 0.8MPa, and the water volume of the boiler is less than 50L).
2. Integral design of high-efficiency energy-saving environment-friendly gas/oil steam boiler
The high-efficiency energy-saving environment-friendly gas/oil steam boiler integrates a boiler body, a burner, a steam drum, a waste heat utilization system and the like, and has the characteristics of small floor area, high heat efficiency and the like through a combined structural design. Furthermore, the external steel frame is arranged, and the whole boiler is designed by a pipe box type structure, so that the air leakage of the boiler can be reduced to the minimum, the air leakage and the heat loss of the boiler are reduced, and the efficiency of the boiler is improved; the boiler adopts a box body external heat insulation structure, an external guard plate is arranged outside the external heat insulation structure to protect heat insulation materials, and the heat dissipation loss is not more than 2%.
3. Water supply system research design
The boiler water level monitoring and early warning device is arranged to monitor the boiler water level, when the water level in the working cavity (namely the inner cavity of the heat exchange tube) is too low, the boiler water feeding pump works to supplement the pumping in the heat preservation water tank into the working cavity, so that the service life of equipment is prevented from being influenced by dry burning of the working cavity, and if the water level in the working cavity is too high, the water supplementing is automatically stopped. When the water in the heat-preservation water tank is used up, a prompting device arranged on the heat-preservation water tank can give out prompting sound and automatically supply water. Through addding holding water box to turn over the automatic control of board level gauge realization system through magnetism, can effectively prevent the problem of water supply in-process system component damage, increased water storage capacity, can effectually avoid the shutdown trouble emergence that the boiler caused because of reasons such as short-term cutting off the water supply.
4. Intelligent explosion-proof design
The explosion-proof device is arranged on the hearth and comprises a door body, a cover plate and an elastic resetting piece of the cover plate, wherein the door body is provided with a gas release hole, the cover plate is arranged on the door body and can block the gas release hole, the cover plate can be far away from the door body under the action of pressure, and after the pressure is relieved, the cover plate can be combined with the door body under the action of the elastic resetting piece to block the gas release hole of the door body. When the burner causes the hearth to explode due to misoperation or other reasons, the explosion-proof device can release and reduce explosion power (pressure) so as to protect the hearth.
5. PID combustor design
The burner is provided with a multivariable PID proportion control system, and can accurately perform proportion loop control on air, pressure (fuel quantity) and water supply quantity, so that the hearth achieves the most efficient combustion effect, high-temperature flue gas passes through an energy saver and a flue gas heat recovery system, is subjected to tail gas purification treatment and then is discharged up to the standard, and the heat efficiency is more than or equal to 93%.
Drawings
FIG. 1 is a schematic longitudinal sectional view of an energy-efficient and environment-friendly gas/oil steam boiler according to the present invention;
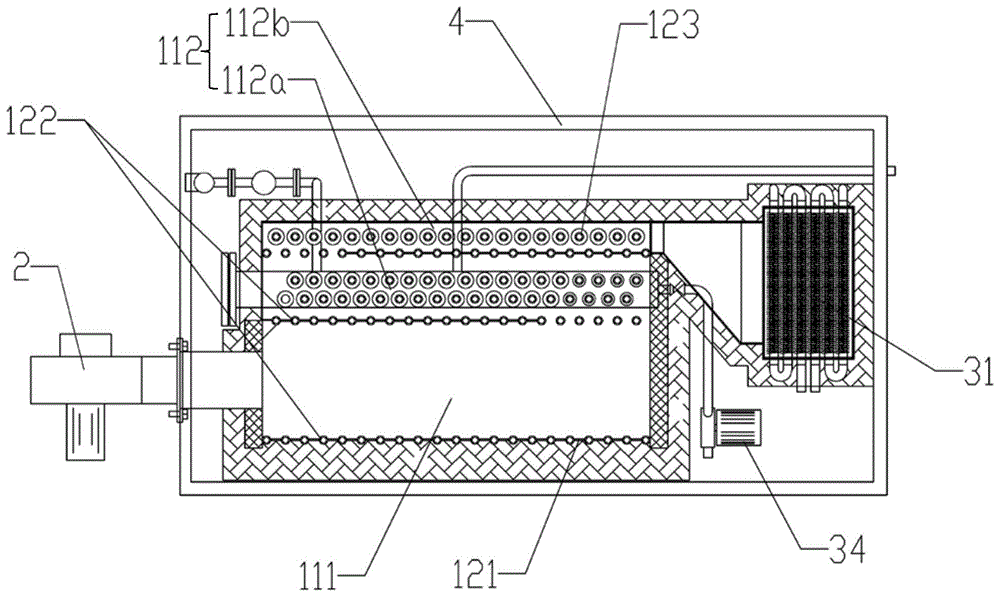
FIG. 2 is a schematic horizontal sectional view of the efficient energy-saving environment-friendly gas/oil steam boiler of the present invention;
FIG. 3 is a schematic cross-sectional view of an efficient energy-saving and environment-friendly gas/oil steam boiler according to the present invention;
FIG. 4 is a schematic view of a water circulation system of the efficient energy-saving environment-friendly gas/oil steam boiler of the invention;
FIG. 5 is a schematic front view of the explosion proof device of the present invention;
fig. 6 is a cross-sectional view of the explosion proof device of the present invention.
Reference numerals
The boiler comprises a boiler body 1, a hearth 11, a combustion zone 111, a convection zone 112, a heat exchange unit 12, a water-cooled wall 121, a first heat exchange pipe 122, a second heat exchange pipe 123, a lower collecting pipe 124, an upper collecting pipe 125, a steam pocket 13, a safety valve 131, a stop valve 132, a furnace wall 14, an explosion-proof device 15, a door body 151, a cover plate 152 and an elastic resetting piece 153; a burner 2; the waste heat utilization system 3, the economizer 31, the circulating water pump 32, the heat preservation water tank 33, the flue gas outlet 311, the multi-loop pipeline 312 and the boiler feed water pump 34; steel frame outsourcing 4; a water level monitoring and early warning device 5, a communication pipe 51 and a magnetic turning plate liquid level meter 52.
Detailed Description
The invention is further described below with reference to specific embodiments and the accompanying drawings. It should be understood that the following examples are illustrative only and are not intended to limit the scope of the present invention.
Example 1
Fig. 1 to 4 show an energy-efficient environment-friendly gas/oil steam boiler according to a preferred embodiment of the present invention, which includes a boiler body 1, a burner 2, a waste heat utilization system 3, and a steel frame outer cover 4.
The boiler body 1 comprises a hearth 11, a heat exchange unit 12, a steam drum 13 and a furnace wall 14; the heat exchange unit 12 comprises a water wall 121, a first heat exchange pipe 122 and a second heat exchange pipe 123, the water wall 121 is longitudinally arranged to divide the hearth 11 into a combustion area 111 and a convection area 112, and the combustion area 111 and the convection area 112 form a loop channel; the first heat exchange tubes 122 are vertically arranged along the interfaces of the two sides of the combustion zone 111 and the convection zone 112, and the water-cooled wall 121 is connected with the first heat exchange tubes 122 in the corresponding area into a whole; the second heat exchange tube 123 is vertically arranged in the convection zone 112; the lower ends of the first heat exchange tube 122 and the second heat exchange tube 123 are converged to a longitudinal lower collecting tube 124, and the upper ends of the first heat exchange tube 122 and the second heat exchange tube 123 are converged to a longitudinal upper collecting tube 125; the steam pocket 13 is arranged at the upper part of the hearth and is communicated with the upper collecting pipe 125 through a vertical pipeline, the steam pocket 13 is provided with a safety valve 131 and a steam conveying pipe, and the steam conveying pipe is provided with a stop valve 132.
The burner 2 is provided at the front end of the boiler body 1 for feeding fuel and oxygen to the combustion zone 111.
The waste heat utilization system 3 comprises an energy saver 31, a circulating water pump 32 and a heat preservation water tank 33, the lower end of the energy saver 31 is positioned at the tail end of the hearth 11 and is communicated with an outlet of the convection zone 112, the upper end of the energy saver 31 is provided with a flue gas outlet 311, a multi-loop pipeline 312 is arranged inside the energy saver 31, and the outside of the energy saver is also preserved by a furnace wall; the multi-loop pipeline 312 is designed by adopting an S-shaped loop curved surface structure, the heat-preservation water tank 33 and the multi-loop pipeline 312 form a water circulation system through a water pipe and provide circulating power by the circulating water pump 32, and water is fed from the upper end of the multi-loop pipeline 312 and discharged from the lower end of the multi-loop pipeline 312; the holding water tank 33 is connected to a lower manifold 124 through a water pipe and a boiler feed pump 34 for supplying water. Preferably, the heat-preserving water tank 33 may be provided therein with a liquid level meter (e.g., a magnetic flap level meter) and a prompting device for monitoring the water level in the heat-preserving water tank to prevent the heat-preserving water tank from running out of water.
Preferably, the second heat exchanging pipe 123 and the multi-loop pipe 312 are fin pipes, which can enhance heat transfer.
Preferably, the lower half part of the multi-loop pipeline 312 is a pressure-bearing section 312a, the upper half part thereof is a normal-pressure section 312b, the wall thickness of the pressure-bearing section 312a is greater than that of the normal-pressure section 312b, and the inner diameter of the pressure-bearing section 312a is smaller than that of the normal-pressure section 312 b. The product is a D-grade boiler, namely a D-grade steam boiler, which means a steam boiler with the steam pressure less than or equal to 0.8MPa and the boiler water volume less than 50L. Therefore, the above two criteria must be met, but the reduction of the water volume means the reduction of the heating area, and it is difficult to meet the requirements of energy saving regulations while meeting the rated evaporation capacity. Therefore, when the product is designed, the specification diameter of the pipe of the pressure-bearing heating surface is reduced, the wall thickness of the pipe of the heating surface is increased, so that the water volume is reduced, and meanwhile, the abundant water volume is used in the tail heating surface, so that a pressure-bearing and normal-pressure combined tail recovery module is designed, and the requirements of the two standards are met.
Preferably, the convection section 112 is divided into two opposite flow channels, wherein two rows of second heat exchange tubes 123 are disposed in the flow channel 112a adjacent to the combustion section, and one row of second heat exchange tubes 123 is disposed in the other flow channel 112 b.
Preferably, the hearth 11 is provided with an explosion-proof device 15, as shown in fig. 5 and 6, the explosion-proof device 15 comprises a door body 151, a cover plate 152 and an elastic resetting piece 153; the door body 151 is fixed on an opening at one end (the tail end of a preferred combustion area) of the hearth 11 through bolts, and the door body 151 is provided with an air release hole; the elastic reset member 153 includes a spring and a spring seat, the spring seat is fixed on the door body 151, the spring is installed in the spring seat, and the outer end of the spring is connected with the cover plate 152, and the spring makes the cover plate 152 cover the door body 151 and blocks the air release hole.
The outside water level monitoring early warning device 5 that is used for monitoring the boiler water level that still is equipped with of boiler body 1, water level monitoring early warning device 5 includes communicating pipe 51 and magnetism and turns over board level gauge 52, and communicating pipe 51 upper end and steam pocket 13 intercommunication, the communicating pipe 51 lower extreme and lower collecting pipe 124 intercommunication, magnetism turn over board level gauge 52 locate on communicating pipe 51 and highly close with last collecting pipe 125. The water level monitoring and early warning device 5 is used for monitoring the water level of the boiler and setting a normal water level a, a lowest safe water level b and a highest safe water level c. When the water level in the working cavity (namely the inner cavity of the heat exchange tube) is too low (lower than the lowest safe water level b), the boiler feed water pump 34 works to supplement the pump in the heat preservation water tank 33 into the working cavity, so that the service life of the equipment is prevented from being influenced by dry burning of the working cavity; and if the water level in the working cavity is too high (higher than the highest safe water level c), the water is automatically stopped to be supplemented. When the water in the heat-preservation water tank 33 is used up, the prompting device arranged on the heat-preservation water tank 33 can give out prompting sound, and water is automatically supplemented into the heat-preservation water tank 33.
The boiler body 1, the economizer 31, the boiler feed pump 34, the water level monitoring and early warning device 5 and the like are wrapped by the steel frame outer bag 4, and the heat preservation water tank and the circulating water pump are arranged outside the steel frame outer bag 4.
The working process is as follows:
the actual work of the boiler is divided into a flue gas system and a steam-water system.
The flow of the flue gas system is as follows: the fuel (such as natural gas) is fully mixed with the air in the combustor 2 and then is completely combusted, the high-temperature flue gas firstly completes radiation heat release in a combustion area 111 of the hearth 11, then enters a convection area 112 (pressure-bearing convection section) to complete primary convection heat release, finally enters an energy saver 31 (normal-pressure convection section) to complete secondary convection heat release, and finally is discharged into the atmosphere through a flue gas outlet.
The steam-water system flow is as follows: the water after water treatment enters the heat preservation water tank, is sent into the energy saver 31 through the circulating water pump, and is preheated through the multi-loop pipeline 311 of the energy saver 31, so that the water temperature is increased and is sent back to the heat preservation water tank, and the flue gas is further subjected to waste heat recovery. Water in the heat-preservation water tank enters the boiler body through a boiler water feeding pump according to a water level signal, is heated to be heated to become saturated steam, enters the steam drum 13, and provides qualified saturated steam for a heat utilization unit through a gas pipe after steam-water separation is realized in the steam drum 13.
The key technology and positive progress effect of the invention are as follows:
1. multi-stage heat exchange design and waste heat utilization system design
In the boiler body 1 of the invention, the hearth 11 is divided into the combustion zone 111 and the convection zone 112, fuel and oxygen can be combusted in the combustion zone 111, and are transferred to the water cooling wall 121 and the first heat transfer pipe 122 through radiation heat transfer, and then fuel gas enters the convection zone 112 and is transferred to the second heat transfer pipe 123 and the water cooling wall 121 and the first heat transfer pipe 122 at the interface through convection heat transfer, so that multi-stage heat exchange is carried out in the hearth 11, heat is efficiently transferred to water in the heat transfer pipes, and the energy conversion efficiency of the hearth is effectively improved. The waste heat utilization system 3 is arranged close to the boiler body 1 and comprises a multi-loop pipeline type energy saver 31, a water circulation system and the like, the waste heat multi-loop pipeline 312 adopts an S-shaped loop curved surface structure design, the heat contact area is increased, dust is not easy to attach, the maximum heat recovery is realized, the process water is preheated by the water circulation system, the heat efficiency is further improved, and the purposes of energy conservation and emission reduction are achieved.
The combustion zone 111, the convection zone 112 and the economizer 31 of the invention can carry out multi-stage heat exchange, not only can strengthen heat exchange, but also is more beneficial to steam pressure adjustment through the adjustment of the front and back water volumes, simultaneously can avoid bursting risk caused by severe change of steam pressure, improves the safety performance of the boiler, and can meet the technical requirements of a D-grade boiler (the steam pressure is less than or equal to 0.8MPa, and the water volume of the boiler is less than 50L).
2. Integral design of high-efficiency energy-saving environment-friendly gas/oil steam boiler
The high-efficiency energy-saving environment-friendly gas/oil steam boiler integrates the boiler body 1, the combustor 2, the steam drum 13, the waste heat utilization system 3 and the like, and has the characteristics of small floor area, high thermal efficiency and the like through a combined structural design. Furthermore, the steel frame outer package 4 is arranged, and the whole boiler is designed by a pipe box type structure, so that the air leakage of the boiler can be reduced to the minimum, the air leakage and the heat loss of the boiler are reduced, and the efficiency of the boiler is improved; the boiler adopts a box body external heat insulation structure, an external guard plate is arranged outside the external heat insulation structure to protect heat insulation materials, and the heat dissipation loss is not more than 2%.
3. Water supply system research design
The invention is provided with a water level monitoring and early warning device 5 to monitor the water level of the boiler, when the water level in the working cavity (namely the inner cavity of the heat exchange tube) is too low, the water feeding pump of the boiler works to pump and supplement the heat preservation water tank into the working cavity, thereby preventing the working cavity from burning dry to influence the service life of the equipment, and if the water level in the working cavity is too high (higher than the highest safe water level c), the water supplement is automatically stopped. When the water in the heat-preservation water tank 33 is used up, the prompting device arranged on the heat-preservation water tank 33 can give out prompting sound and automatically supply water. Through addding holding water box to turn over the automatic control of board level gauge realization system through magnetism, can effectively prevent the problem of water supply in-process system component damage, increased water storage capacity, can effectually avoid the shutdown trouble emergence that the boiler caused because of reasons such as short-term cutting off the water supply.
4. Intelligent explosion-proof design
The invention sets up the explosion-proof apparatus 15 on the burner hearth, the explosion-proof apparatus includes the door body, cover plate and elastic reset piece of the cover plate, there are air release holes on the door body, the cover plate is set up on the door body can block the air release hole, the cover plate can be kept away from the door body under the function of pressure, can combine with the door body and block the air release hole of the door body under the function of elastic reset piece after the pressure is relieved. When the burner causes the hearth to explode due to misoperation or other reasons, the explosion-proof device can release and reduce explosion power (pressure) so as to protect the hearth.
5. PID combustor design
The burner is provided with a multivariable PID proportion control system, and can accurately perform proportion loop control on air, pressure (fuel quantity) and water supply quantity, so that the hearth achieves the most efficient combustion effect, high-temperature flue gas passes through an energy saver and a flue gas heat recovery system, is subjected to tail gas purification treatment and then is discharged up to the standard, and the heat efficiency is more than or equal to 93%.