A ripples sword rough milling cutter for processing of cast iron vortex dish
Technical Field
The invention relates to the technical field of milling cutter structures, in particular to a wave edge rough milling cutter for machining a cast iron scroll.
Background
As a new fluid machine, a scroll compressor has been widely used in the fields of air conditioning refrigeration, gas compression, engine supercharging, vacuum pump, etc. due to its advantages of compact structure, high efficiency of operation, low noise, and stability. The scroll plate is the most central component of the scroll compressor, and the processing precision of the scroll plate directly influences the working performance of the scroll compressor. At present, the workpiece material of the scroll plate mainly comprises alloy cast iron and aluminum alloy, and the cutting manufacturability is poor due to the material performance characteristics. Meanwhile, the complex profile structure of the scroll is also an important factor influencing the cutting quality and precision of the scroll.
The milling cutter is a main cutter for machining the turbine disc, and for rough milling machining of a turbine disc blank precast groove, the cutter is plunged and cut into the turbine disc blank from the center of the scroll disc and then rotates along a scroll path for cutting. Because the turbine disc blank pre-casting groove is deep, a milling cutter with a larger long diameter needs to be selected, and the cutting of the cutter is mostly full cutting; when the milling cutter rotates along the vortex path for cutting, the end edge and the peripheral edge of the milling cutter need to process two side surfaces and the groove bottom surface of the vortex disc at the same time, so that the forward milling and the backward milling are alternately carried out during the cutting of the milling cutter; meanwhile, the cutting tool often generates phenomena of breakage and breakage of the cutting edge, breakage of the cutting tool and the like due to factors such as mechanical impact, cutting vibration and uneven cutting stress; in addition, due to the elastic-plastic deformation of the cutting layer metal, the friction between the cutter and a workpiece and chips is large, the cutting temperature is high, and the phenomena of chip accumulation, bonding damage and the like of the cutter are caused due to high temperature, so that the service life of the cutter is influenced.
For the processing of the cast iron scroll, because the alloy elements of the material are more (such as chromium is less than or equal to 0.25 percent and nickel is less than or equal to 3 percent), the hardness of the workpiece is relatively higher (HB 201-255), and according to the technical characteristics of full-cutter cutting, the conventional milling cutter processing has the disadvantages of high cutting difficulty, serious cutter abrasion and short cutter service life. Therefore, it is necessary to design a rough milling cutter with a wavy edge for machining a cast iron scroll to solve the problems of cutting vibration and large impact load of the cutter, so as to improve the cutting efficiency and prolong the service life of the cutter
Disclosure of Invention
In view of the above problems, the present invention provides a roughing milling cutter with a wavy edge for machining a cast iron scroll, which improves cutting efficiency and tool durability and prolongs the tool life.
A kind of rough milling cutter of wave blade used for processing the cast iron vortex disc, it includes clamping shank of the cutting tool, cutting edge and transition neck, the said transition neck is used for connecting the clamping shank of the said cutting tool and cutting edge; the method is characterized in that: the tool clamping handle part is a cylindrical straight handle; cutting edge includes a plurality of cutting edges and the chip groove of arranging spirally, N cutting edge ring cloth under the cross section state in the outer ring week of cutting edge arranges, and wherein N is more than or equal to 3's natural number, the chip groove is located the ring periphery that forms behind the adjacent cutting edge combination and corresponds the interval region intra-area, including chip breaker groove, chip groove in the chip groove, the chip groove is equipped with tank bottom surface and knife face, every the cutting edge comprises end sword, week sword and the knife tip R angle that is used for connecting end sword and week sword, and end sword and week sword front end part are equipped with rake face and straight back knife face, are equipped with the circular arc tooth that is sinusoidal waveform on the week sword.
It is further characterized in that: the milling cutter tool material adopts 10 percent of cobalt content and K with fracture toughnessICHigh ultra-fine grain cemented carbide;
the diameter of the tool clamping handle part is larger than or equal to that of the cutting edge part;
the value of N is 4, 5 and 6;
the diameter d2 of the cutting edge part is 10 mm-20 mm, the edge length l of the cutting edge part is 3-4 times of the diameter d2, and the core thickness d0 of the cutting edge part is 70% of the diameter d 2;
the radius R of the tool nose R angle of the cutting edge part is 0.3 mm-0.5 mm;
the end edge concave angle of the cutting edge part is 1 degree;
first relief angle alpha of end edge and peripheral edge of cutting edge part1Is 10 to 12 degrees and a second relief angle alphao1Is 18 degrees to 20 degrees;
the angle of the helical angle beta of the cutter is 35-40 degrees;
a rake angle gamma of the peripheral edge of the cutting edge part o10 to 14 degrees;
the length f of the peripheral edge of the cutting edge part from the end edgeo>The wave making blade is not arranged at the position of 2mm, and the wave making part of the peripheral blade is provided with arc teeth in sine wave shape;
the wave-shaped structure of the peripheral edge is in sine periodic change, the wave-shaped circular arc tooth is formed by tangently transitionally connecting two sections of circular arcs, and the radius of the wave crest circular arc of the wave-shaped circular arc tooth is R1The radius of the arc of the trough is R2;
The grinding spiral direction of the wave edge is the same as the spiral direction of the groove of the cutter;
after the cutter wave-shaped circular arc tooth rotates for a circle, the wave shapes are mutually superposed, and the cutting width is equal to a wave edge lead (or called tooth pitch) Lo
Compared with the common end milling cutter, the wave edge milling cutter has the advantages that the cutting edge is a wave-shaped curved surface with a variable helical angle, and the arc-shaped cutter teeth not only can reduce the load of the cutter, but also have higher impact resistance. The wave edge milling cutter cuts a workpiece by a convex peak firstly during cutting, the cutting is easy, the cutting is light and fast, the load is stable, the vibration is small, the elastic deformation of the cutter is small, the friction force is small, the cutting edge is not easy to wear, and the wave edge milling cutter is more suitable for processing hard and tough materials.
Drawings
FIG. 1 is a schematic front view of the present invention;
FIG. 2 is a right side view of the cutting edge of the present invention;
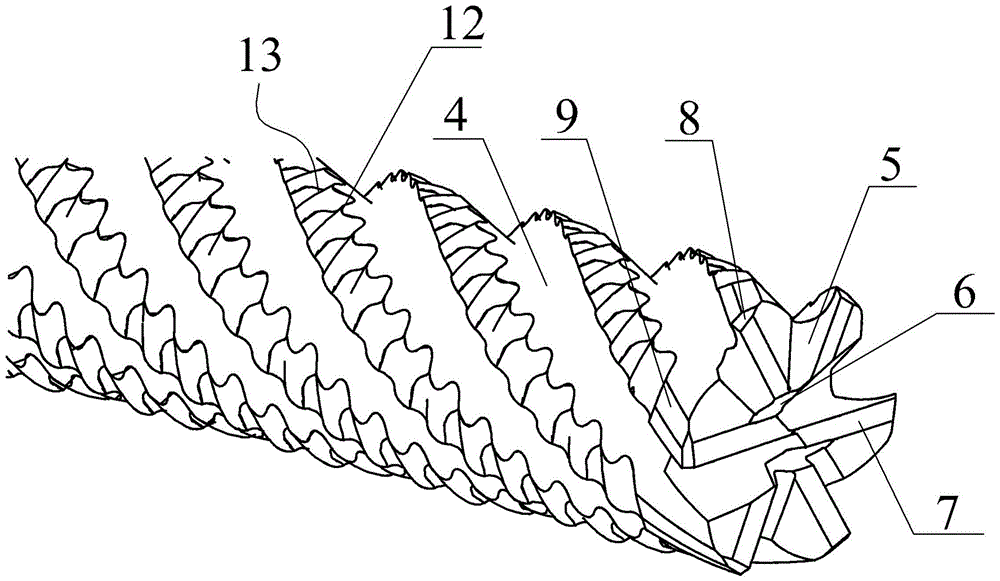
FIG. 3 is a schematic perspective view of a cutting edge according to the present invention;
FIG. 4 is a partial cross-sectional structural view of the peripheral edge of the cutting edge of the present invention;
FIG. 5 is a wave-like schematic view of the peripheral edge of the cutting edge of the present invention;
the names corresponding to the sequence numbers in the figure are as follows:
the cutting edge part 1, the transition neck part 2, the tool clamping handle part 3, the chip groove 4, the chip breaker groove 6, the chip breaker groove 5, the end edge 7, the tool nose R angle 8, the peripheral edge 9, the front tool face 10, the straight back tool face 11, the circular arc tooth 12 and the cutting edge 13.
Detailed Description
A wave edge roughing mill for machining cast iron scrolls, see fig. 1-5: the cutting tool comprises a tool clamping handle part 3, a cutting edge part 1 and a transition neck part 2, wherein the transition neck part 2 is used for connecting the tool clamping handle part 3 and the cutting edge part 1; the cutter clamping handle part 3 is a cylindrical straight handle; the cutting edge part 1 comprises a plurality of cutting edges 13 and chip discharge grooves 4 which are spirally arranged, the N cutting edges 13 are annularly distributed on the periphery of the outer ring of the cutting edge part 1 in a cross section state, wherein N is a natural number which is more than or equal to 3, the chip discharge grooves 4 are positioned in the corresponding interval areas of the periphery formed by combining the adjacent cutting edges 13, the chip discharge grooves 4 comprise chip breakers 6 and chip grooves 5, the chip grooves 5 are provided with groove bottom surfaces and a cutter face, each cutting edge 13 comprises an end edge 7, a peripheral edge 9 and a cutter nose R angle 8 which is used for connecting the end edge 7 with the peripheral edge 9, the front end parts of the end edge 7 and the peripheral edge 9 are provided with a front cutter face 10 and a straight rear cutter face 11, and the peripheral edge 9 is provided with a circular arc tooth 12 which is.
The milling cutter tool material adopts 10 percent of cobalt content and K with fracture toughnessICHigh ultra-fine grain cemented carbide;
the diameter of the tool holding shank 3 is greater than or equal to the diameter of the cutting edge 1;
the value of N is 4, 5 and 6;
peripheral edge rake angle gamma of cutting edge part 1o10 to 14 degrees;
the length f of the peripheral edge of the cutting edge part from the end edgeo>The 2mm position is not provided with a wave making blade, and the wave making part of the peripheral blade is provided with arc teeth 12 in sine wave shape;
the wave structure of the cutting peripheral edge is in sine periodic change, the wave-shaped circular arc tooth is formed by tangently transitionally connecting two sections of circular arcs, and the wave crest circular arc radius of the wave-shaped circular arc tooth is R1The radius of the arc of the trough is R2;
The grinding spiral direction of the wave edge is the same as the spiral direction of the groove of the cutter;
after the cutter wave-shaped circular arc tooth rotates for a circle, the wave shapes are mutually superposed, and the cutting width is equal to a wave edge lead (or called tooth pitch) Lo
In the specific implementation: the number of cutting edges of the cutting edge part 1 is generally 4-6, and the diameter d2 of the cutting edge part 1 is 10-20 mm; however, since the more the milling cutter teeth, the more the grooves, the more the rigidity and strength of the cutter itself are reduced, and the wave edge milling cutter is often used for full cutting in heavy load machining, the cutting edge length l of the cutting edge portion 1 is generally 3 to 4 times the diameter d2, and the core thickness d0 of the cutting edge portion 1 is generally 70% of the diameter d2, in order to ensure the rigidity of the wave edge milling cutter and the stability of the cutting process.
The intersection lines of the chip grooves 4 and 6 and the solid part of the cutter form a plurality of cutting edges; the cutting edges are uniformly distributed in the radial direction relative to the center of the front end surface of the cutting edge part 1; wherein, the cutting edge is composed of an end edge 7, a peripheral edge 9 and a tool nose R angle 8 for connecting the end edge and the peripheral edge, the radius R of the tool nose R angle is generally set to be 0.3 mm-0.5 mm; the cutter point R angle 8 greatly improves the cutter point strength of the joint of the end edge 7 and the peripheral edge 9, effectively reduces or eliminates the possibility of tipping of the cutter point of the cutter, enhances the cutting performance of the cutter and prolongs the service life of the cutter; the end edge concave angle of the cutting edge part 1 is set to be 1 degree, so that the end face of the milling cutter can be effectively prevented from being collided with the bottom surface of a workpiece, and cutting and chip removal are facilitated; the end edge 7 and the peripheral edge 9 are provided at the tip with a rake face 10 and a straight flank face 11, and the first relief angle α of the end edge 7 and the peripheral edge 9 of the cutting edge part 1 is set to overcome the friction between the flank faces of the tool end edge 7 and the peripheral edge 9 and the cutting surface1Set to 10-12 DEG, and a second relief angle alphao1Is 18-20 degrees. Due to the material characteristics of the cast iron turbine disc, in order to improve the rigidity, cutting and chip removal performance of the cutter, the angle beta of the helical angle of the cutter is generally set to be 35-40 degrees; with simultaneous tool helix angle beta and rake angle gammaoClosely related, the larger the helix angle β, the anterior angle γoThe larger the cutting distortion, the smaller the peripheral rake angle γ of the cutting edge portion 1oIs set to 10 to 14 degrees.
In order to ensure sufficient strength of the tool end cutting edge 7 for the manufacture of the peripheral cutting edge wave-shaped circular arc teeth of the wave cutting edge milling cutter, the length f of the peripheral cutting edge 9 which does not produce waves must be ensured in the portion close to the end cutting edge 7o>2 mm; the wave making part of the peripheral edge 9 is provided with arc teeth in sine wave shape; the wave-shaped structure of the peripheral edge 9 is in sine periodic change, the wave-shaped circular arc tooth is formed by tangently transitionally connecting two sections of circular arcs, and the radius of the wave crest circular arc of the wave-shaped circular arc tooth is R1The radius of the arc of the trough is R2(ii) a The grinding spiral direction of the wave edge is the same as the spiral direction of the groove of the cutter; the wave forms of the cutter after the wave form circular arc tooth rotates for one circle are mutually superposed, and the cutting width is equal to one wave edge guideDistance (or pitch) Lo
At present, for the wave making technology of the existing wave blade milling cutter, the spiral direction of the wave blade is opposite to the spiral direction of the groove, namely the groove is made into right-handed rotation, and the wave blade is made into left-handed rotation. However, as for rough milling processing of the pre-cast groove of the cast iron turbine disc blank, experiments prove that, as shown in table 1, taking a 6-blade rough milling cutter with a cutting edge part 1 with a diameter of 11.15mm and a nose R angle with a radius R of 0.3mm as an example, compared with different-blade wave-making grinding modes, when the grinding spiral direction of the wave blade is the same as the spiral direction of the groove of the cutter, the service life of the cutter is improved by about 30% compared with that of the wave-making milling cutter of the existing wave-making mode, so that the reasonability and reliability of the design of the wave-making rough milling cutter are fully explained, the rough milling processing efficiency of the pre-cast groove of the alloy cast iron turbine disc blank can be effectively improved, and the service life of the cutter.
TABLE 1
It will be evident to those skilled in the art that the invention is not limited to the details of the foregoing illustrative embodiments, and that the present invention may be embodied in other specific forms without departing from the spirit or essential attributes thereof. The present embodiments are therefore to be considered in all respects as illustrative and not restrictive, the scope of the invention being indicated by the appended claims rather than by the foregoing description, and all changes which come within the meaning and range of equivalency of the claims are therefore intended to be embraced therein. Any reference sign in a claim should not be construed as limiting the claim concerned.
Furthermore, it should be understood that although the present description refers to embodiments, not every embodiment may contain only a single embodiment, and such description is for clarity only, and those skilled in the art should integrate the description, and the embodiments may be combined as appropriate to form other embodiments understood by those skilled in the art.