CN112123032A - Magnetic particle grinding device and process for machining inner wall of conical part - Google Patents
Magnetic particle grinding device and process for machining inner wall of conical part Download PDFInfo
- Publication number
- CN112123032A CN112123032A CN202011127138.XA CN202011127138A CN112123032A CN 112123032 A CN112123032 A CN 112123032A CN 202011127138 A CN202011127138 A CN 202011127138A CN 112123032 A CN112123032 A CN 112123032A
- Authority
- CN
- China
- Prior art keywords
- magnetic pole
- electric cylinder
- workpiece
- magnetic
- ultrasonic vibration
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B1/00—Processes of grinding or polishing; Use of auxiliary equipment in connection with such processes
- B24B1/005—Processes of grinding or polishing; Use of auxiliary equipment in connection with such processes using a magnetic polishing agent
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B1/00—Processes of grinding or polishing; Use of auxiliary equipment in connection with such processes
- B24B1/04—Processes of grinding or polishing; Use of auxiliary equipment in connection with such processes subjecting the grinding or polishing tools, the abrading or polishing medium or work to vibration, e.g. grinding with ultrasonic frequency
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B41/00—Component parts such as frames, beds, carriages, headstocks
- B24B41/06—Work supports, e.g. adjustable steadies
- B24B41/061—Work supports, e.g. adjustable steadies axially supporting turning workpieces, e.g. magnetically, pneumatically
- B24B41/062—Work supports, e.g. adjustable steadies axially supporting turning workpieces, e.g. magnetically, pneumatically between centres; Dogs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B47/00—Drives or gearings; Equipment therefor
- B24B47/10—Drives or gearings; Equipment therefor for rotating or reciprocating working-spindles carrying grinding wheels or workpieces
- B24B47/12—Drives or gearings; Equipment therefor for rotating or reciprocating working-spindles carrying grinding wheels or workpieces by mechanical gearing or electric power
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B49/00—Measuring or gauging equipment for controlling the feed movement of the grinding tool or work; Arrangements of indicating or measuring equipment, e.g. for indicating the start of the grinding operation
- B24B49/12—Measuring or gauging equipment for controlling the feed movement of the grinding tool or work; Arrangements of indicating or measuring equipment, e.g. for indicating the start of the grinding operation involving optical means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B51/00—Arrangements for automatic control of a series of individual steps in grinding a workpiece
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
- Constituent Portions Of Griding Lathes, Driving, Sensing And Control (AREA)
Abstract
本发明的目的在于提供一种用于加工锥形零件内壁的磁粒研磨装置及工艺,装置包括机床、外部磁极装置、内部超声波振动磁极装置,所述外部磁极装置设置在工件外部,并能够通过机床上的第一滑台驱动沿工件轴向移动;所述内部超声波振动磁极装置与工件同轴,并能够通过机床上的第二滑台驱动将辅助磁极送入工件内部。本发明可实现对锥型类内壁进行光整加工。能够提高工件表面质量和使用寿命,有效提升研磨速度和研磨质量。
The purpose of the present invention is to provide a magnetic particle grinding device and process for machining the inner wall of a conical part, the device includes a machine tool, an external magnetic pole device, and an internal ultrasonic vibration magnetic pole device, the external magnetic pole device is arranged outside the workpiece, and can pass through The first sliding table on the machine tool is driven to move along the axial direction of the workpiece; the internal ultrasonic vibration magnetic pole device is coaxial with the workpiece, and can be driven by the second sliding table on the machine tool to send the auxiliary magnetic pole into the workpiece. The invention can realize the finishing process on the inner wall of the cone type. It can improve the surface quality and service life of the workpiece, and effectively improve the grinding speed and grinding quality.
Description
技术领域technical field
本发明涉及磁粒研磨与光整加工技术领域,尤其涉及一种用于加工锥形零件内壁的磁粒研磨装置及工艺。The invention relates to the technical field of magnetic particle grinding and finishing, in particular to a magnetic particle grinding device and a process for processing the inner wall of a conical part.
背景技术Background technique
在机械化、自动化不断发展的今天,锥形类零件的应用变得尤为广泛。漏斗是锥形类较为最典型的代表,其内壁的表面质量对加工效率和加工成本有着直接影响。因为锥形零件特有的形状原因,在对其进行磁粒研磨时需要不断调整外部磁极与零件外表面间的距离,使得磁极与磨料间形成闭合的磁回路,进而研磨到所需的加工精度。这种操作不仅费时费力而且效率极低,因此发明一种专门用于加工锥形类零件的装置尤为重要。With the continuous development of mechanization and automation, the application of conical parts has become particularly extensive. The funnel is the most typical representative of the conical type, and the surface quality of its inner wall has a direct impact on the processing efficiency and processing cost. Due to the unique shape of tapered parts, the distance between the outer magnetic pole and the outer surface of the part needs to be adjusted continuously when magnetic particle grinding is performed, so that a closed magnetic circuit is formed between the magnetic pole and the abrasive, and then the required machining accuracy is achieved. This operation is not only time-consuming and labor-intensive, but also extremely inefficient, so it is particularly important to invent a device specially designed for processing tapered parts.
中国专利CN111168483A公开了一种非导磁同心变径管内表面磁粒研磨方法及装置。此装置利用滑片组的移动从而调节磁铁至加工工件外表面的距离,但该装置结构复杂、安装要求高、且加工精度差。Chinese patent CN111168483A discloses a method and device for grinding magnetic particles on the inner surface of a non-magnetically conductive concentric reducing tube. The device utilizes the movement of the sliding vane group to adjust the distance between the magnet and the outer surface of the workpiece to be processed, but the device has a complex structure, high installation requirements, and poor machining accuracy.
发明内容SUMMARY OF THE INVENTION
本发明的目的在于提供一种用于加工锥形零件内壁的磁粒研磨装置及工艺,可实现对锥型类内壁进行光整加工。能够提高工件表面质量和使用寿命,有效提升研磨速度和研磨质量。The purpose of the present invention is to provide a magnetic particle grinding device and a process for processing the inner wall of a conical part, which can realize the finishing process of the inner wall of the conical type. It can improve the surface quality and service life of the workpiece, and effectively improve the grinding speed and grinding quality.
为实现上述目的,本发明采用以下技术方案实现:To achieve the above object, the present invention adopts the following technical solutions to realize:
一种用于加工锥形零件内壁的磁粒研磨装置,包括机床、外部磁极装置、内部超声波振动磁极装置,所述外部磁极装置设置在工件外部,并能够通过机床上的第一滑台驱动沿工件轴向移动;所述内部超声波振动磁极装置与工件同轴,并能够通过机床上的第二滑台驱动将辅助磁极送入工件内部。A magnetic particle grinding device for machining the inner wall of a conical part, comprising a machine tool, an external magnetic pole device, and an internal ultrasonic vibration magnetic pole device, the external magnetic pole device is arranged outside the workpiece, and can be driven by a first sliding table on the machine tool along the The workpiece moves axially; the inner ultrasonic vibration magnetic pole device is coaxial with the workpiece, and can drive the auxiliary magnetic pole into the workpiece through the second sliding table on the machine tool.
所述内部超声波振动磁极装置包括超声波发生器、转换器、集电环、变幅杆、球头连杆、辅助磁极、超声振动装置固定座,所述的转换器、集电环和变幅杆安装在超声波发生器上,所述辅助磁极通过球头连杆安装在变幅杆上,所述超声波发生器安装在超声振动装置固定座上,所述超声振动装置固定座安装在第二滑台上。The internal ultrasonic vibration magnetic pole device includes an ultrasonic generator, a converter, a collector ring, a horn, a ball-head connecting rod, an auxiliary magnetic pole, an ultrasonic vibration device holder, the converter, the collector ring and the horn. Installed on the ultrasonic generator, the auxiliary magnetic pole is installed on the horn through the ball joint connecting rod, the ultrasonic generator is installed on the ultrasonic vibration device holder, and the ultrasonic vibration device holder is installed on the second sliding table superior.
所述外部磁极装置包括电动缸、红外测距传感器,所述红外测距传感器安装在电动缸端部的磁极上。The external magnetic pole device includes an electric cylinder and an infrared distance measuring sensor, and the infrared distance measuring sensor is installed on the magnetic pole at the end of the electric cylinder.
所述电动缸包括磁极、电动缸丝杠、电动缸套筒、电动缸螺母、电动缸推杆、电动缸轴承、电动缸减速器、电动缸伺服电机,所述电动缸丝杠通过电动缸轴承安装在电动缸套筒中,所述电动缸螺母螺接在电动缸丝杠上、并能够沿着电动缸套筒内壁滑动,所述电动缸推杆的一端与电动缸螺母固定连接,电动缸推杆的另一端伸出电动缸套筒与磁极固定连接,在电动缸推杆与电动缸套筒之间设有导向套,所述电动缸伺服电机通过电动缸减速器传动连接电动缸丝杠。The electric cylinder includes a magnetic pole, an electric cylinder screw, an electric cylinder sleeve, an electric cylinder nut, an electric cylinder push rod, an electric cylinder bearing, an electric cylinder reducer, and an electric cylinder servo motor, and the electric cylinder screw passes through the electric cylinder bearing. Installed in the electric cylinder sleeve, the electric cylinder nut is screwed on the electric cylinder screw and can slide along the inner wall of the electric cylinder sleeve, one end of the electric cylinder push rod is fixedly connected with the electric cylinder nut, and the electric cylinder The other end of the push rod protrudes from the electric cylinder sleeve and is fixedly connected to the magnetic pole. A guide sleeve is arranged between the electric cylinder push rod and the electric cylinder sleeve. The electric cylinder servo motor is connected to the electric cylinder lead screw through the electric cylinder reducer. .
所述工件是非导磁金属锥形管件。The workpiece is a non-magnetically conductive metal conical pipe.
一种用于加工锥形零件内壁的磁粒研磨装置的研磨工艺,具体方法如下:A grinding process of a magnetic particle grinding device for processing the inner wall of a conical part, the specific method is as follows:
1)用三角卡盘将所加工金属管工件固定在机床上,将磁性磨料放入工件内部,移动第一滑台,使外部磁极装置的磁极置于工件的初始研磨位置,移动第二滑台使内部超声波振动磁极装置的辅助磁极进入到工件内部并与所述磁极相对,使其形成闭合磁场;1) Fix the processed metal pipe workpiece on the machine tool with a triangular chuck, put the magnetic abrasive into the workpiece, move the first sliding table, make the magnetic pole of the external magnetic pole device at the initial grinding position of the workpiece, and move the second sliding table Make the auxiliary magnetic pole of the internal ultrasonic vibration magnetic pole device enter the inside of the workpiece and be opposite to the magnetic pole to form a closed magnetic field;
2)设定磁极与工件外表面的距离,使工作后磁极始终能够保持与工件表面间的距离恒定;再将超声振动产生的振幅加在辅助磁极上;2) Set the distance between the magnetic pole and the outer surface of the workpiece, so that the magnetic pole can always keep the distance between the magnetic pole and the surface of the workpiece constant after work; then add the amplitude generated by the ultrasonic vibration to the auxiliary magnetic pole;
3)启动机床电机,实现三角卡盘带动工件完成与机床主轴同转速的旋转运动;3) Start the machine tool motor to realize that the triangular chuck drives the workpiece to complete the rotational movement at the same speed as the machine tool spindle;
4)使溜板箱a和溜板箱b同步运动,以保证内部辅助磁极与磁极始终形成闭合磁场,带动磁性磨料进行研磨;4) Make the sliding box a and the sliding box b move synchronously to ensure that the internal auxiliary magnetic pole and the magnetic pole always form a closed magnetic field, and drive the magnetic abrasive to grind;
5)利用红外测距传感器实时测量磁极与工件的距离,通过测量信号的反馈,使磁极能够在沿着锥形工件轴向移动的过程中进行伸缩,从而保证磁极与工件表面的距离,达到最佳研磨效果。5) Use the infrared distance measuring sensor to measure the distance between the magnetic pole and the workpiece in real time, and through the feedback of the measurement signal, the magnetic pole can expand and contract during the axial movement of the conical workpiece, so as to ensure the distance between the magnetic pole and the workpiece surface to achieve the maximum Excellent grinding effect.
与现有的技术相比,本发明的有益效果是:Compared with the prior art, the beneficial effects of the present invention are:
本发明是一种用于加工各种尺寸锥形零件的装置,可根据工件不同的精度要求,在PLC系统中先行设置磁极与工件表面的距离,加工精度高时,可将二者之间的距离值设置较小,为磨料提供较大的研磨压力。加工精度低时,可将距离值设置的大些,避免过度加工。在加工过程中,红外测距传感器通过信号的接收,将所测距离输入到PLC系统中,系统根据所设定的参数值驱动电动缸将磁极带到指定位置,以保证磁极与工件表面间的距离。本装置中的超声振动和辅助磁极部分,超声振动装置为辅助磁极提供一个水平方向的振动,使得工件内部的磁性磨料产生高频振动,提高研磨速度,与此同时增强了磁性磨粒翻滚更新的性能,从而提高研磨效率,改善工件的内表面质量。辅助磁极的存在,缩短了磁极间的距离,从而增大磁感应强度,提高了研磨速度和研磨质量。The invention is a device for processing conical parts of various sizes. According to the different precision requirements of the workpiece, the distance between the magnetic pole and the surface of the workpiece can be set in advance in the PLC system. When the machining accuracy is high, the distance between the two can be adjusted. A smaller distance value setting provides greater grinding pressure for the abrasive. When the machining accuracy is low, the distance value can be set larger to avoid excessive machining. In the process of processing, the infrared distance measuring sensor inputs the measured distance into the PLC system through the reception of the signal, and the system drives the electric cylinder to bring the magnetic pole to the designated position according to the set parameter value, so as to ensure the distance between the magnetic pole and the workpiece surface. distance. The ultrasonic vibration and auxiliary magnetic pole part in this device, the ultrasonic vibration device provides a horizontal vibration for the auxiliary magnetic pole, which makes the magnetic abrasive inside the workpiece generate high-frequency vibration, improves the grinding speed, and at the same time enhances the tumbling and renewal of the magnetic abrasive particles. performance, thereby increasing the grinding efficiency and improving the inner surface quality of the workpiece. The existence of auxiliary magnetic poles shortens the distance between the magnetic poles, thereby increasing the magnetic induction intensity and improving the grinding speed and grinding quality.
附图说明Description of drawings
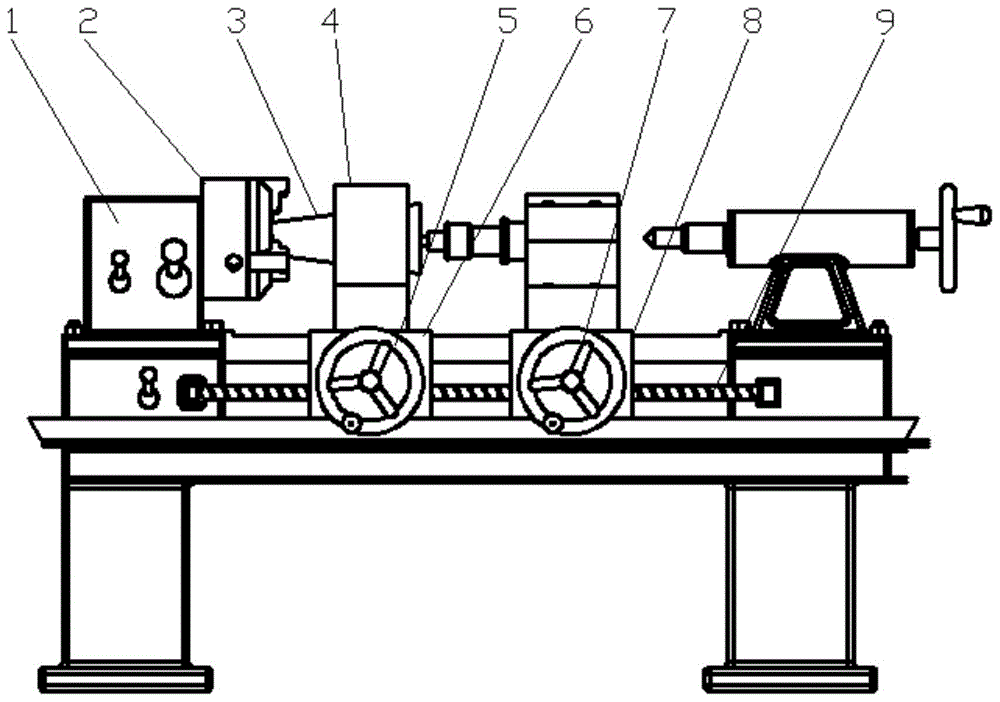
图1是本发明的整体结构示意图。FIG. 1 is a schematic diagram of the overall structure of the present invention.
图2是本发明的结构示意俯视图。FIG. 2 is a schematic top view of the structure of the present invention.
图3是本发明的超声振动部分的结构示意图。FIG. 3 is a schematic view of the structure of the ultrasonic vibration part of the present invention.
图4是图3的左视图。FIG. 4 is a left side view of FIG. 3 .
图5是本发明电动缸控制部分的结构示意图。FIG. 5 is a schematic diagram of the structure of the electric cylinder control part of the present invention.
图中:1-机床 2-三角卡盘 3-工件 4-电动缸放置架 5-手轮Ⅰ 6-溜板箱a 7-手轮Ⅱ 8-溜板箱b 9-丝杠 10-控制手柄 11-电动缸 12-红外测距传感器 13-第一滑台 14-第二滑台 15-超声振动装置固定座 16-超声波发生器 17-转换器 18-集电环 19-变幅杆20-球头连杆 21-辅助磁极 22-磁极 23-电动缸导向套 24-电动缸丝杠 25-电动缸套筒26-电动缸螺母 27-电动缸伺服电机 28-电动缸轴承 29-电动缸减速器 30-电动缸推杆。In the figure: 1-machine tool 2-triangular chuck 3-workpiece 4-electric cylinder placement frame 5-handwheel Ⅰ 6-slide box a 7-handwheel Ⅱ 8-slide box b 9-lead screw 10-control handle 11-electric cylinder 12-infrared distance measuring sensor 13-first slide 14-second slide 15-ultrasonic vibration device holder 16-ultrasonic generator 17-converter 18-collecting ring 19-amplifier 20- Ball head connecting rod 21- Auxiliary magnetic pole 22- Magnetic pole 23- Electric cylinder guide sleeve 24- Electric cylinder screw 25- Electric cylinder sleeve 26- Electric cylinder nut 27- Electric cylinder servo motor 28- Electric cylinder bearing 29- Electric cylinder deceleration 30 - electric cylinder push rod.
具体实施方式Detailed ways
下面对本发明做详细说明,但本发明的实施范围不仅仅限于下述的实施方式。The present invention will be described in detail below, but the scope of implementation of the present invention is not limited to the following embodiments.
如图1-图5所示,一种用于加工锥形零件内壁的磁粒研磨装置,包括机床1、外部磁极装置、内部超声波振动磁极装置,所述外部磁极装置设置在工件3外部,并能够通过机床1上的第一滑台13驱动沿工件3轴向移动;所述内部超声波振动磁极装置与工件3同轴,并能够通过机床1上的第二滑台14驱动将辅助磁极21送入工件3内部。As shown in Figures 1-5, a magnetic particle grinding device for processing the inner wall of a conical part includes a machine tool 1, an external magnetic pole device, an internal ultrasonic vibration magnetic pole device, and the external magnetic pole device is arranged outside the workpiece 3, and It can be driven by the first sliding table 13 on the machine tool 1 to move in the axial direction of the workpiece 3; the internal ultrasonic vibration magnetic pole device is coaxial with the workpiece 3, and can be driven by the second sliding table 14 on the machine tool 1 to send the auxiliary
所述内部超声波振动磁极装置包括超声波发生器16、转换器17、集电环18、变幅杆19、球头连杆20、辅助磁极21、超声振动装置固定座15,所述的转换器17、集电环18和变幅杆19安装在超声波发生器16上,所述辅助磁极21通过球头连杆20安装在变幅杆19上,所述超声波发生器16安装在超声振动装置固定座15上,所述超声振动装置固定座15安装在第二滑台14上。The internal ultrasonic vibration magnetic pole device includes an
所述外部磁极装置包括电动缸11、红外测距传感器12,所述红外测距传感器12安装在电动缸11端部的磁极22上。The external magnetic pole device includes an
所述电动缸11包括磁极22、电动缸丝杠25、电动缸套筒25、电动缸螺母26、电动缸推杆30、电动缸轴承28、电动缸减速器29、电动缸伺服电机27,所述电动缸丝杠24通过电动缸轴承28安装在电动缸套筒25中,所述电动缸螺母26螺接在电动缸丝杠24上、并能够沿着电动缸套筒25内壁滑动,所述电动缸推杆30的一端与电动缸螺母26固定连接,电动缸推杆30的另一端伸出电动缸套筒25与磁极22固定连接,在电动缸推杆30与电动缸套筒25之间设有导向套23,所述电动缸伺服电机27通过电动缸减速器29传动连接电动缸丝杠24。The
所述工件3是非导磁金属锥形管件。The workpiece 3 is a non-magnetic conductive metal conical pipe.
本发明的外部磁极装置在工件直径变化的情况下,可以始终保证磁极22与工件3间的最佳距离。内部超声波振动磁极装置使得磨料具有更为复杂的运动轨迹,内部辅助磁极可增强磁感应强度,达到更好的研磨效果。The external magnetic pole device of the present invention can always ensure the optimal distance between the
安装在磁极22上的红外测距传感器12通过红外信号来测量磁极22与工件3的距离,进而将指令传给PLC控制器,它作为位置反馈装置,用于实时反馈电动缸推杆30位置。电动缸推杆30头部连接磁极22,通过电动缸推杆30的运动,进而改变磁极22与工件3间的距离,以保证达到最佳的研磨效果。PLC控制器发送指令给伺服电机驱动器,伺服电机驱动器根据指令驱动电动缸伺服电机27运转,通过电动缸减速器29带动电动缸丝杠24旋转;电动缸螺母26径向定位,在电动缸丝杠24旋转力矩驱动下与电动缸推杆30一起做往复直线运动,电动缸推杆30头部连接磁极22,通过电动缸推杆30的运动,进而改变磁极22与工件3间的距离。在开始加工前根据加工精度的不同要求,提前在PLC系统中设置好磁极22与工件3间的最佳距离,既可以提供足够的研磨压力又可避免过度加工。The infrared ranging
超声振动装置通过球头连杆20与内部辅助磁极21相连,为辅助磁极21提供一个水平方向的振动,使得金属管工件3内部的磁性磨料产生高频振动,提高研磨速度,与此同时增强了磁性磨粒翻滚更新的性能,从而提高研磨效率,改善金属管的内表面质量。The ultrasonic vibration device is connected with the internal auxiliary
超声波发生器16将交流电信号转换成为超声频的电振荡信号,换能器17将超声频的电振荡信号转变为同频的机械振动信号,通过集电环18将机械振动信号收集起来,经过变幅杆19将微小的振动幅值放大,再经过球头连杆20,最终将振动传给内部辅助磁极21,使其做径向超声振动,使得磨料的运动轨迹更为复杂,研磨效果更佳,改善工件3的内表面质量。与此同时增强了磁性磨粒翻滚更新的性能,提高了磨料的自锐性,从而提高研磨效率。The
一种用于加工锥形零件内壁的磁粒研磨装置的研磨工艺,具体方法如下:A grinding process of a magnetic particle grinding device for processing the inner wall of a conical part, the specific method is as follows:
1)用三角卡盘将所加工金属管工件3固定在机床1上,将磁性磨料放入工件3内部,移动第一滑台13,使外部磁极装置的磁极22置于工件3的初始研磨位置,移动第二滑台14使内部超声波振动磁极装置的辅助磁极21进入到工件3内部并与所述磁极22相对,使其形成闭合磁场;1) Fix the processed metal pipe workpiece 3 on the machine tool 1 with a triangular chuck, put the magnetic abrasive into the workpiece 3, move the first sliding table 13, and place the
2)根据工件3精度要求自行在PLC控制系统中设定磁极22与工件3外表面的距离,使工作后磁极22始终能够保持与工件3表面间的距离恒定;再将超声振动产生的振幅加在辅助磁极21上,在此作用下提高了磨料的振动频率,带动磨料灵活地翻滚,更好地完成切削刃自锐,进而加工质量和加工效率;2) Set the distance between the
3)启动机床1电机,实现三角卡盘带动工件3完成与机床1主轴同转速的旋转运动;3) Start the motor of the machine tool 1 to realize that the triangular chuck drives the workpiece 3 to complete the rotational movement at the same speed as the spindle of the machine tool 1;
4)使溜板箱a6和溜板箱b8同步运动,以保证内部辅助磁极21与磁极22始终形成闭合磁场,带动磁性磨料进行研磨;4) Synchronous movement of the sliding box a6 and the sliding box b8 to ensure that the internal auxiliary
5)利用红外测距传感器12实时测量磁极21与工件3的距离,通过测量信号的反馈,使磁极21能够在沿着锥形工件3轴向移动的过程中进行伸缩,从而保证磁极21与工件3表面的距离,达到最佳研磨效果。5) Using the infrared
以上所述,仅为本发明较佳的具体实施方式,但本发明的保护范围并不局限于此,任何熟悉本技术领域的技术人员在本发明揭露的技术范围内,根据本发明的技术方案及其发明构思加以等同替换或改变,都应涵盖在本发明的保护范围之内。The above description is only a preferred embodiment of the present invention, but the protection scope of the present invention is not limited to this. The equivalent replacement or change of the inventive concept thereof shall be included within the protection scope of the present invention.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011127138.XA CN112123032A (en) | 2020-10-20 | 2020-10-20 | Magnetic particle grinding device and process for machining inner wall of conical part |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011127138.XA CN112123032A (en) | 2020-10-20 | 2020-10-20 | Magnetic particle grinding device and process for machining inner wall of conical part |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN112123032A true CN112123032A (en) | 2020-12-25 |
Family
ID=73853895
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202011127138.XA Pending CN112123032A (en) | 2020-10-20 | 2020-10-20 | Magnetic particle grinding device and process for machining inner wall of conical part |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN112123032A (en) |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007268689A (en) * | 2006-03-31 | 2007-10-18 | Utsunomiya Univ | Magnetic polishing apparatus, magnetic polishing method, and machining tool used for them |
| CN208289551U (en) * | 2018-05-17 | 2018-12-28 | 辽宁科技大学 | A kind of quartz glass pipe internal surface ultrasound magnetic force multiple grinding device |
| CN109866085A (en) * | 2019-04-12 | 2019-06-11 | 辽宁科技大学 | A kind of multiple grinding precision tube apparatus and polishing process |
| CN111266936A (en) * | 2020-03-20 | 2020-06-12 | 辽宁科技大学 | A kind of electromagnet composite ultrasonic magnetic grinding device and using method thereof |
| CN213702730U (en) * | 2020-10-20 | 2021-07-16 | 辽宁科技大学 | A magnetic particle grinding device for machining the inner wall of conical parts |
-
2020
- 2020-10-20 CN CN202011127138.XA patent/CN112123032A/en active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007268689A (en) * | 2006-03-31 | 2007-10-18 | Utsunomiya Univ | Magnetic polishing apparatus, magnetic polishing method, and machining tool used for them |
| CN208289551U (en) * | 2018-05-17 | 2018-12-28 | 辽宁科技大学 | A kind of quartz glass pipe internal surface ultrasound magnetic force multiple grinding device |
| CN109866085A (en) * | 2019-04-12 | 2019-06-11 | 辽宁科技大学 | A kind of multiple grinding precision tube apparatus and polishing process |
| CN111266936A (en) * | 2020-03-20 | 2020-06-12 | 辽宁科技大学 | A kind of electromagnet composite ultrasonic magnetic grinding device and using method thereof |
| CN213702730U (en) * | 2020-10-20 | 2021-07-16 | 辽宁科技大学 | A magnetic particle grinding device for machining the inner wall of conical parts |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN203236309U (en) | Magnetic grinding device for synchronously polishing inner surface and outer surface of straight pipe | |
| CN203918724U (en) | A kind of bend pipe inner surface magnetic grinding polishing machine | |
| CN106938410A (en) | The burnishing device and its method of big L/D ratio internal surface of elongated tube | |
| CN109571159B (en) | A kind of free abrasive micro ultrasonic processing device and feed adjustment method | |
| CN203109722U (en) | Supersonic vibration internal grinding device | |
| CN106826403A (en) | A kind of automatic fine grinding device in shaft-like workpiece outer surface | |
| CN208289551U (en) | A kind of quartz glass pipe internal surface ultrasound magnetic force multiple grinding device | |
| CN205520756U (en) | Handle of a knife integrated system suitable for high -speed supersound mills and grinds processing | |
| CN111266936A (en) | A kind of electromagnet composite ultrasonic magnetic grinding device and using method thereof | |
| CN205363431U (en) | A compound polishing processingequipment of supersound magnetic force for free -form surface part | |
| CN102152238B (en) | Grinding processing method and device for online grinding wheel dressing by ultrasonic vibration and | |
| CN103273386B (en) | The auxiliary fine ultrasonic machine tool of a kind of electrophoresis and processing method | |
| CN109866085A (en) | A kind of multiple grinding precision tube apparatus and polishing process | |
| CN103920953A (en) | Universal ultrasonic-assisted inner jetted dielectric electric discharge machining (EDM) milling tool head and manufacturing method thereof | |
| CN105033780A (en) | Deep cavity machining system suitable for crisp and hard materials | |
| CN104889888B (en) | A kind of grinder wheel control by permanent velocity system and control method | |
| CN105666254A (en) | Controllable multi-dimensional ultrasonic ELID composite internal grinding test device | |
| CN108436751A (en) | Pipe fitting internal hole vertical fine grinding device | |
| CN107953203A (en) | A kind of device and technique for being used to refine helicla flute | |
| CN203292952U (en) | Electrophoresis-assisted micro ultrasonic machining tool | |
| CN206632769U (en) | The burnishing device of big L/D ratio internal surface of elongated tube | |
| CN109514358B (en) | A profile-constrained ultrasonic vibration-assisted rotary abrasive streamer finishing device | |
| CN205438028U (en) | Automatic circle multidimension ultrasonic vibration and compound grinding test device of ELID in controlization | |
| CN213702730U (en) | A magnetic particle grinding device for machining the inner wall of conical parts | |
| CN105643463A (en) | Ultrasonic vibration cup-shaped grinding wheel dresser for dressing super-hard abrasive grinding wheel |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20201225 |
|
| RJ01 | Rejection of invention patent application after publication |