CN112060423A - Beryllium-copper-material-based mold conformal waterway and preparation method and application thereof - Google Patents
Beryllium-copper-material-based mold conformal waterway and preparation method and application thereof Download PDFInfo
- Publication number
- CN112060423A CN112060423A CN202011007551.2A CN202011007551A CN112060423A CN 112060423 A CN112060423 A CN 112060423A CN 202011007551 A CN202011007551 A CN 202011007551A CN 112060423 A CN112060423 A CN 112060423A
- Authority
- CN
- China
- Prior art keywords
- beryllium copper
- mold
- copper material
- waterway
- pipe body
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 239000000463 material Substances 0.000 title claims abstract description 117
- 238000002360 preparation method Methods 0.000 title abstract description 7
- DMFGNRRURHSENX-UHFFFAOYSA-N beryllium copper Chemical compound [Be].[Cu] DMFGNRRURHSENX-UHFFFAOYSA-N 0.000 claims abstract description 106
- 238000000034 method Methods 0.000 claims abstract description 53
- 238000003466 welding Methods 0.000 claims abstract description 50
- 238000009792 diffusion process Methods 0.000 claims abstract description 43
- 238000001816 cooling Methods 0.000 claims abstract description 36
- 238000003754 machining Methods 0.000 claims abstract description 12
- 238000004519 manufacturing process Methods 0.000 claims abstract description 11
- 238000012545 processing Methods 0.000 claims description 20
- 238000012546 transfer Methods 0.000 claims description 14
- 239000003292 glue Substances 0.000 claims description 9
- 238000010438 heat treatment Methods 0.000 claims description 8
- 238000001746 injection moulding Methods 0.000 claims description 8
- 238000009434 installation Methods 0.000 claims description 5
- 238000004321 preservation Methods 0.000 claims description 5
- 238000000465 moulding Methods 0.000 claims description 3
- 238000003825 pressing Methods 0.000 claims description 2
- 229910000831 Steel Inorganic materials 0.000 abstract description 23
- 239000010959 steel Substances 0.000 abstract description 23
- 239000002994 raw material Substances 0.000 abstract 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 26
- 230000000694 effects Effects 0.000 description 10
- 238000010586 diagram Methods 0.000 description 9
- 238000013461 design Methods 0.000 description 7
- 230000008901 benefit Effects 0.000 description 4
- 230000017525 heat dissipation Effects 0.000 description 4
- 238000002347 injection Methods 0.000 description 4
- 239000007924 injection Substances 0.000 description 4
- 238000007789 sealing Methods 0.000 description 4
- 239000000243 solution Substances 0.000 description 4
- 238000004458 analytical method Methods 0.000 description 3
- 238000005219 brazing Methods 0.000 description 3
- 229910052751 metal Inorganic materials 0.000 description 3
- 239000002184 metal Substances 0.000 description 3
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 description 2
- 238000004891 communication Methods 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000005457 optimization Methods 0.000 description 2
- 230000002093 peripheral effect Effects 0.000 description 2
- 238000007639 printing Methods 0.000 description 2
- 239000007787 solid Substances 0.000 description 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 1
- LFQSCWFLJHTTHZ-UHFFFAOYSA-N Ethanol Chemical compound CCO LFQSCWFLJHTTHZ-UHFFFAOYSA-N 0.000 description 1
- 125000000174 L-prolyl group Chemical group [H]N1C([H])([H])C([H])([H])C([H])([H])[C@@]1([H])C(*)=O 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000000205 computational method Methods 0.000 description 1
- 239000000110 cooling liquid Substances 0.000 description 1
- 239000000498 cooling water Substances 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 239000010949 copper Substances 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000012938 design process Methods 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 239000007789 gas Substances 0.000 description 1
- 238000009776 industrial production Methods 0.000 description 1
- 238000011900 installation process Methods 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 229910052757 nitrogen Inorganic materials 0.000 description 1
- 238000005498 polishing Methods 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- -1 specifically Substances 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C33/00—Moulds or cores; Details thereof or accessories therefor
- B29C33/38—Moulds or cores; Details thereof or accessories therefor characterised by the material or the manufacturing process
- B29C33/3835—Designing moulds, e.g. using CAD-CAM
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C33/00—Moulds or cores; Details thereof or accessories therefor
- B29C33/38—Moulds or cores; Details thereof or accessories therefor characterised by the material or the manufacturing process
- B29C33/3842—Manufacturing moulds, e.g. shaping the mould surface by machining
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/72—Heating or cooling
- B29C45/73—Heating or cooling of the mould
- B29C45/7312—Construction of heating or cooling fluid flow channels
- B29C2045/7318—Construction of heating or cooling fluid flow channels multilayered fluid channel constructions
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Fluid Mechanics (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
Abstract
The invention relates to the technical field of dies, and particularly discloses a beryllium copper material-based die conformal waterway, a preparation method and application thereof, wherein the die conformal waterway is manufactured by adopting beryllium copper material and comprises a pipe body arranged in the die, the pipe body is of a multilayer pipeline structure, two adjacent layers of pipeline structures are communicated in a diffusion welding mode, and one end of the pipe body is provided with a plurality of connecting ports which are respectively communicated with corresponding parts of the pipe body in a diffusion welding mode; the provided preparation method is high in operability, the mold conformal water channel manufactured by taking the beryllium copper material as the raw material and adopting the diffusion welding process has better connection strength and service life, meanwhile, the cooling efficiency can be optimized, the method can be used for mass production, and the problems that the conformal water channel of the traditional mold system is mostly made of steel and processed by the traditional machining mode, or the beryllium copper material is processed by the traditional welding process, and the cooling efficiency is low are solved.
Description
Technical Field
The invention relates to the technical field of molds, in particular to a beryllium copper material-based mold conformal water channel and a preparation method and application thereof.
Background
In the existing market, in the production and manufacturing industry, the die system can be generally applied, and the die system is known as an industrial banknote printing machine and has important significance for industrial production. Generally, the free-form water path is a part structure designed in a mold to improve a heat dissipation effect. In the prior art, most of the mould shape-following waterway parts are made of mould steel, beryllium copper materials are used as non-standard parts, and a cooling waterway with a traditional drilling process structure is adopted. Beryllium copper material has better heat conductivity than mould steel, and traditional mould system for the optimization of considering the radiating efficiency can be with separating out the difficult cooling position when designing, and cool down with beryllium copper material substitution mould steel, the mould system heat conduction efficiency that adopts this kind of structure can improve to some extent but can't reach optimization effect.
Therefore, the above technical solution also has the following disadvantages in practical use: the shape following water channel of the traditional mould system is mostly made of steel and processed by the traditional machining mode, or beryllium copper is used for processing by the traditional welding process, so that the shape following water channel part with high reliability cannot be manufactured, and the problem of low cooling efficiency exists.
Disclosure of Invention
The embodiment of the invention aims to provide a beryllium copper material-based mold conformal water channel, which is used for solving the problem that the conventional mold system provided in the background art is processed by adopting steel materials and relying on the conventional machining mode, or is processed by adopting a beryllium copper material and adopting the conventional welding process, so that the cooling efficiency is low.
The embodiment of the invention is realized in such a way that the beryllium copper material-based mold conformal water channel is manufactured by adopting the beryllium copper material, and the beryllium copper material-based mold conformal water channel specifically comprises the following steps:
the pipe body is arranged in the die and used for transmitting a heat transfer medium so as to regulate the temperature of the die, the pipe body is of a multilayer pipeline structure, and adjacent two layers of pipeline structures are connected in a diffusion welding mode to form a communicating structure; and
and the connecting ports are arranged at one end of the pipe body, are a plurality of and are respectively communicated with the corresponding parts of the pipe body in a diffusion welding mode so as to realize the inlet and outlet of the heat transfer medium, and are communicated with the outside of the mould.
In another embodiment of the present invention, a method for preparing the beryllium copper material-based mold conformal waterway is further provided, where the method for preparing the beryllium copper material-based mold conformal waterway specifically includes the following steps:
drawing the die by using 3D drawing software to obtain a three-dimensional modeling image, and calculating the three-dimensional modeling image by using finite element analysis software to obtain a 3D drawing file of the beryllium copper material-based die shape-following water channel with optimal cooling efficiency;
the method comprises the steps that a 3D drawing file is manufactured in a layered entity mode through beryllium copper materials to obtain a pipe body and a plurality of connectors, the pipe body is of a multilayer pipeline structure, then two adjacent layers of pipeline structures are connected in a diffusion welding mode to form a communicating structure, and meanwhile the connectors are respectively communicated with corresponding positions of the pipe body in a diffusion welding mode to form an integral structure;
and carrying out shape processing on the integral structure so as to meet the installation and use requirements of the die.
In another embodiment of the invention, the mold conformal water channel based on the beryllium copper material is prepared by the method for preparing the mold conformal water channel based on the beryllium copper material.
In another embodiment of the invention, the application of the beryllium copper material-based mold conformal water channel in mold processing is further provided.
In another embodiment of the invention, the application of the preparation method of the mold conformal waterway based on the beryllium copper material in the processing of the beryllium copper material product is also provided.
Compared with the prior art, the invention has the beneficial effects that:
the beryllium copper material-based mould is manufactured by adopting a beryllium copper material along with a shape water path, and specifically comprises a pipe body arranged in the mould and used for transmitting a heat transfer medium to regulate the temperature of the mould, wherein the pipe body is of a multilayer pipeline structure, two adjacent layers of pipeline structures are connected in a diffusion welding mode to form a communication structure, one end of the pipe body is provided with a plurality of connecting ports which are respectively communicated with corresponding parts of the pipe body in a diffusion welding mode to realize the inlet and outlet of the heat transfer medium, and the connecting ports are communicated with the outside of the mould; the preparation method of the beryllium copper material-based mold conformal waterway is high in operability, the beryllium copper material-based mold conformal waterway which is manufactured by adopting the diffusion welding process is designed by using the optimized cooling scheme, compared with the brazing or other welding processes, the mold conformal waterway has better connection strength and service life, and meanwhile, the cooling efficiency can be optimized, so that the method can be used for mass production, and the problems that the conventional mold system conformal waterway is processed by adopting steel materials and relying on the conventional machining mode, or the beryllium copper material is processed by adopting the conventional welding process, the cooling efficiency is not high are solved, and the method has a wide market prospect.
Drawings
Fig. 1 is a perspective view of a conventional die made of steel according to the prior art.
Fig. 2 is a schematic bottom structure view of a conventional die made of steel according to the prior art.
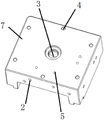
Fig. 3 is a schematic structural diagram of a mold manufactured by beryllium copper material for mounting the beryllium copper material-based mold conformal water channel according to an embodiment of the present invention.
Fig. 4 is a schematic bottom structure diagram of a mold made of beryllium copper material for mounting the beryllium copper material-based mold conformal water channel according to an embodiment of the invention.
Fig. 5 is a schematic structural view of a beryllium copper material-based mold conformal water channel according to another embodiment of the present invention.
Fig. 6 is a schematic bottom structure view of a beryllium copper material-based mold conformal waterway according to another embodiment of the present invention.
Fig. 7 is a schematic structural diagram of a conformal waterway component made of steel according to another embodiment of the present invention.
Fig. 8 is a schematic cross-sectional view illustrating a mold following waterway installed in a mold based on beryllium copper according to another embodiment of the present invention.
Fig. 9 is a layered schematic view of a beryllium copper material-based mold conformal waterway according to another embodiment of the present invention.
Fig. 10 is a layered schematic view of a mold for mounting a mold form-following waterway based on beryllium copper material according to another embodiment of the present invention.
In the figure: 1-a first mounting hole; 2-water channel water sealing hole; 3-injection molding a glue inlet; 4-a second mounting hole; 5-water path inlet and outlet holes; 6-connecting port; 7-a mold body; 8-a pipe body.
Detailed Description
In order to make the technical problems, technical solutions and advantages of the present invention more apparent, the present invention will be further described in detail with reference to the accompanying drawings and specific embodiments. The following examples will assist those skilled in the art in further understanding the invention, but are not intended to limit the invention in any way. It should be noted that variations and modifications can be made by persons skilled in the art without departing from the spirit of the invention. All falling within the scope of the present invention. In order to make the technical solution of the present invention clearer, process steps and device structures well known in the art are omitted here.
In the description of the present invention, it is to be understood that the terms "upper", "lower", "front", "rear", "left", "right", "top", "bottom", "inner", "outer", and the like, indicate orientations or positional relationships based on the orientations or positional relationships shown in the drawings, are merely for convenience in describing the present invention and simplifying the description, and do not indicate or imply that the device or element being referred to must have a particular orientation, be constructed and operated in a particular orientation, and thus, should not be construed as limiting the present invention. Furthermore, the terms "first", "second", etc. are used for descriptive purposes only and are not to be construed as indicating or implying relative importance or implicitly indicating the number of technical features indicated. Thus, a feature defined as "first," "second," etc. may explicitly or implicitly include one or more of that feature. In the description of the present invention, "a plurality" means two or more unless otherwise specified.
Specific implementations of the present invention are described in detail below with reference to specific embodiments.
Firstly, as shown in fig. 1-2, a structure diagram of a conventional mold made of steel in the prior art is provided, a conformal waterway component made of steel is arranged in the conventional mold, and a specific structure of the conformal waterway component made of steel is shown in fig. 7.
Referring to fig. 1-2 specifically, the conventional mold made of steel comprises a mold main body 7, and an injection glue inlet 3 is arranged at the axis of the mold main body 7, the injection glue inlet 3 is used for injecting a material into the conventional mold for processing and forming, the mold main body 7 is further provided with a plurality of first mounting holes 1 and a plurality of second mounting holes 4 for mounting the conformal water path parts made of steel, specifically, the first mounting holes 1 can adopt hoisting screw holes, the second mounting holes 4 can adopt part fixing screw holes, the bottom of the mold main body 7 is correspondingly provided with a plurality of water path inlet and outlet holes 5, the water path inlet and outlet holes 5 are communicated with the bottom outlet of the conformal water path parts made of steel, the side surface of the mold main body 7 is correspondingly provided with a plurality of water path water sealing holes 2 communicated with the horizontal outlet of the conformal water path parts made of steel, so as to realize the inlet and outlet of the heat transfer medium, and the structure is more complex.
In another embodiment, as shown in fig. 5 to 6, a structural diagram of a mold conformal waterway based on a beryllium copper material is provided for an embodiment of the present invention, where the mold conformal waterway based on the beryllium copper material is manufactured by using the beryllium copper material, and specifically includes:
the pipe body 8 is arranged inside the die and used for transmitting a heat transfer medium to adjust the temperature of the die, the pipe body 8 is of a multilayer pipeline structure, and two adjacent layers of pipeline structures are connected in a diffusion welding mode to form a communicating structure; and
and a plurality of connectors 6 arranged at one end of the pipe body 8, wherein the connectors 6 are respectively communicated with corresponding parts of the pipe body 8 in a diffusion welding mode to realize the inlet and outlet of the heat transfer medium, and the connectors 6 are communicated with the outside of the mold.
In the embodiment of the invention, the shape following water path is designed inside the beryllium copper material die to achieve the optimal cooling effect by combining the performance advantage of the beryllium copper material with the diffusion welding process, and the main parts of the die are changed from the manufacturing process of die steel and the beryllium copper material into the manufacturing of pure beryllium copper material.
In an example of the present invention, the heat transfer medium may be a fluid, such as a gas or a liquid, specifically, water, alcohol, nitrogen, freon, and the like, and when water is used, a cooling effect may be achieved, and when freon is used, a freon refrigerator in the prior art may be referred to, so as to achieve a cooling effect.
It should be noted that the beryllium copper material-based mold shape following water path enables the cooling flow channel to be more attached to a heating area by means of a diffusion welding connection process, no redundant structure is provided, the cooling liquid can flow out of the product more quickly, the heat is reduced more quickly, an optimal cooling effect is achieved, the cost of using diffusion welding is slightly higher, and the structure and the cooling effect of the cooling system are optimal. Referring to fig. 8, the cross-sectional view of the mold conformal waterway based on the beryllium copper material is shown after being installed in the mold, the central semicircular line is in the shape of the mold, the conformal waterway structure is in a circular shape, and the optimal position of the conformal waterway can be seen from the figure so as to realize the optimal cooling efficiency.
Referring to fig. 3-4, in an example of the present invention, the mold is made of beryllium copper, and specifically includes a mold main body 7, and an injection glue inlet 3 is disposed at an axial center of the mold main body 7, and the injection glue inlet 3 is used for injecting a material into the mold for machine-shaping. Still be provided with on the mould main part 7 and be used for the installation a plurality of first mounting hole 1 and a plurality of second mounting hole 4 of body 8 are specific, hoist and mount screw hole can be adopted to first mounting hole 1, second mounting hole 4 can adopt the fixed screw hole of part. The outer wall of one side of the die main body 7 close to the connecting port 6 is correspondingly provided with a plurality of water path inlet and outlet holes 5, and the water path inlet and outlet holes 5 are communicated with the corresponding connecting port 6 so as to realize the inlet and outlet of the heat transfer medium.
In the embodiment of the invention, compared with the traditional mold, the beryllium copper material mold reduces the water channel water sealing holes 2 on the side, the material is different from the appearance observation, the structure is different, and the drill bit can reduce redundant structural characteristics for the mold.
An embodiment of the present invention further provides a method for preparing the beryllium copper material-based mold conformal water channel, where the method for preparing the beryllium copper material-based mold conformal water channel specifically includes the following steps:
drawing the die by using 3D drawing software to obtain a three-dimensional modeling image, and calculating the three-dimensional modeling image by using finite element analysis software to obtain a 3D drawing file of the beryllium copper material-based die shape-following water channel with optimal cooling efficiency;
the 3D drawing file is manufactured by adopting beryllium copper materials in a layered entity mode to obtain a pipe body 8 and a plurality of connecting ports 6, the pipe body 8 is of a multilayer pipeline structure, then the adjacent two layers of pipeline structures are connected in a diffusion welding mode to form a communicating structure, and meanwhile the connecting ports 6 are respectively communicated with the corresponding parts of the pipe body 8 in a diffusion welding mode to form an integral structure;
and carrying out shape processing on the integral structure so as to meet the installation and use requirements of the die.
Further, in an example of the present invention, the method for preparing the beryllium copper material-based mold conformal waterway specifically includes the following steps:
designing a mold according to the product processing requirement, selecting a material of an injection molding part as a beryllium copper material when designing the mold, drawing the mold by using 3D drawing software to obtain a three-dimensional modeling image (as shown in figures 3 and 4), and analyzing and calculating a heating area of the mold represented by the three-dimensional modeling image in work by using finite element analysis software after the design is finished to obtain a 3D diagram file (as shown in figures 5 and 6) of the mold conformal water path based on the beryllium copper material with optimal cooling efficiency; the main heating area of the die can be achieved through finite element analysis software, a shape-following water path is designed for the area, the shape of the heating area is semicircular, the shape of the shape-following water path is also circular in a surrounding mode, the shape-following water path is not designed to be too close to or too far away from the heating area of the part, the part is cooled too fast due to too close, the product can generate defects, and the cooling efficiency cannot achieve the optimal effect due to too far away;
the 3D picture file is manufactured by layering solid bodies through beryllium copper materials to obtain a pipe body 8 and a plurality of connecting ports 6, the pipe body 8 is of a multilayer pipeline structure, specifically, as shown in fig. 9, the pipe body is a layering schematic diagram of the beryllium copper material-based mould conformal water channel, dotted lines in the layering schematic diagram of the beryllium copper material-based mould conformal water channel represent layering from three positions of the conformal water channel structure, after the conformal water channel is processed, the pipe structures of all layers are assembled and connected in a diffusion welding mode, specifically, the adjacent two layers of pipe structures are connected in the diffusion welding mode to form a communicating structure, and meanwhile, the plurality of connecting ports 6 are respectively communicated with corresponding positions of the pipe body 8 in the diffusion welding mode to form an integral structure;
and after the welding is finished, carrying out shape processing to meet the requirements of the installation and the use of the die, and specifically, carrying out high-precision machining to obtain a solid part which accords with the 3D design. And assembling the die system after all parts of the die system are prepared.
In one example of the present invention, the pipe body 8 is a multi-layer pipe structure, and correspondingly corresponds to a plurality of layers when being installed in a mold, and is a layered schematic diagram of a mold for installing the beryllium copper material based mold conformal water channel, as shown in fig. 10, wherein dotted lines indicate that the layers are formed from three positions of the mold.
In yet another example of the present invention, the diffusion welding mode comprises the following operation steps: the method comprises the steps of attaching and heating a plurality of parts to be diffusion welded to 750-810 ℃, then carrying out heat preservation for 3-6 hours, applying pressure of 6-20 MPa to the plurality of parts during the heat preservation, keeping the pressure for 3-6 hours, and cooling.
In yet another example of the present invention, the shape processing is a high precision machining of the welded beryllium copper material part (integral structure), and the high precision machining mainly processes the mechanical characteristics required by the beryllium copper material part in design: such as the processing of product shapes such as an ejector rod hole of an ejection structure, the processing of an injection molding glue inlet flow passage, the peripheral shape of a product and the like, and the beryllium copper material mold system formed by the beryllium copper material-based mold conformal waterway and the mold can be used for reasonably producing finished products.
In another example of the present invention, the shape of the overall structure is any one of a rectangular parallelepiped, a cube, a cylinder, etc., and the specific shape is selected according to the requirement, which is not limited herein, and the embodiment is mainly illustrated by the cylinder structure shown in fig. 5.
In yet another example of the present invention, the finite element analysis is a modern computational method that has rapidly developed based on structural mechanics analysis, and common general finite element software includes LUSAS, MSC. Nastran, Ansys, Abaqus, LMS-Samtech, Algor, Femap/NX, Nastran, Hypermesh, COMSOL, Multiphysics, FEPG, and the like. The selection is specifically performed according to the requirements, and is not limited herein.
In yet another example of the present invention, the 3D mapping software is of many kinds, such as: 3Dsmax, rhono, cinema 4D, zbrush, poser, maya, Softiimage XSI 5.01, Pro/E, UG, AutoCAD, and the like, and is specifically selected according to the requirements, and is not limited herein.
Further, as a preferred embodiment of the present invention, the method for preparing the beryllium copper material-based mold conformal waterway includes:
1. 3D water path design is carried out on the main forming parts of the beryllium copper material die by using 3D drawing software, and meanwhile, a scheme water path for optimizing the cooling efficiency is calculated by using finite element analysis software, so that the beryllium copper material parts achieve the optimized cooling scheme in the design theory.
2. According to the designed 3D drawing file (three-dimensional modeling drawing file) of the beryllium copper material die part, in order to meet the requirements of the diffusion welding connection process, layered entity manufacturing is carried out, and the layered water channel is processed according to the 3D drawing file, so that plates in one layer are obtained. And (3) starting mechanical processing on the plates subjected to the layering treatment, processing a flow channel of the conformal water channel in the design process, and paying attention to the surface quality of each plate during the processing process.
3. And (3) connecting the machined plates by a diffusion welding method, mainly controlling the temperature and time of parts: and heating the beryllium copper material to 750-810 ℃, then preserving heat, controlling the heat preservation time to be 3-6 hours, applying 6-20 megapascals (Mpa) to the part in the period, keeping the pressure for 3-6 hours, and finishing the diffusion welding process connection after the part is cooled. The connection strength and the sealing strength of the beryllium copper material die part are ensured.
4. All the plates are connected by diffusion welding to form a whole, and the shape of the whole is cuboid, cube, cylinder and other structures. At this time, the welded beryllium copper material part needs to be machined with high precision. The high-precision machining mainly processes the mechanism characteristics required by beryllium copper material parts during design: such as the processing of the shape of the product, such as the ejection structure ejector rod hole, the processing of the injection molding glue inlet flow channel, the peripheral shape of the product and the like. The beryllium copper material die system can be ensured to be capable of producing finished products reasonably.
5. The beryllium copper material die is arranged in a die system along with the shape of the waterway part, and the copper material die base plate is fixed in the corresponding position of the die by the designed screw hole position. The parts are prevented from being collided and damaged in the installation process.
In the embodiment of the invention, the application occasions of the beryllium-copper material die shape-following waterway parts, cooling structure feasibility analysis, machining performance, polishing performance, diffusion welding connection technology process, metal thermal deformation control and other specific processes needing to be used are mastered by combining the five-point technical solution.
The embodiment of the invention provides a beryllium copper material-based mold conformal water channel which is manufactured by adopting a beryllium copper material, and specifically comprises a pipe body 8 arranged in the mold and used for transmitting a heat transfer medium to adjust the temperature of the mold, wherein the pipe body 8 is of a multi-layer pipeline structure, two adjacent layers of pipeline structures are connected in a diffusion welding mode to form a communication structure, one end of the pipe body 8 is provided with a plurality of connecting ports 6 which are respectively communicated with corresponding parts of the pipe body 8 in a diffusion welding mode to realize the inlet and outlet of the heat transfer medium, the connecting ports 6 are communicated with the outside of the mold, the beryllium copper material-based mold conformal water channel manufacturing method is provided, the beryllium copper material-based mold conformal water channel part which is manufactured by adopting a diffusion welding process is designed by using an optimized cooling scheme, compared with brazing or other welding processes, the connecting strength and the service life are better, the cooling efficiency can be optimized, the die can be used for mass production, and the problems that steel is adopted in the conventional die system along with the shape water path and is processed in a conventional machining mode, or beryllium copper is adopted to be processed through the conventional welding process, and the cooling efficiency is not high are solved.
It should be noted that, the main forming parts of the traditional mold system are processed by the cooling waterway flow channel by the traditional machining method, the traditional mold steel material parts can also have a cooling system with good heat dissipation efficiency by using the diffusion welding process, and the beryllium copper material parts cannot be manufactured into the shape following waterway parts with high reliability because the diffusion welding process is not available. The cooling water channel processing can be carried out only by the traditional processing mode, and though the heat conductivity of the beryllium copper material is better than that of the die steel material, the beryllium copper material is not an optimal cooling scheme.
The beryllium copper material mould conformal waterway part manufactured by adopting the diffusion welding process has an optimized cooling scheme, and the design scheme of high heat conductivity of the beryllium copper material and high degree of freedom of the conformal waterway can efficiently take away heat generated in the moulding process of the mould system. The die system does not generate metal fatigue due to high temperature, and has longer service life and higher economic benefit. The beryllium copper material die conformal water channel parts can achieve mechanical properties similar to those of parent metal through a diffusion welding process connection method, and compared with brazing or other welding processes, the beryllium copper material die conformal water channel parts have better connection strength and service life by adopting the diffusion welding process, and meanwhile, the cooling efficiency can also be optimized. Moreover, because the die system is known as an industrial banknote printing machine, the beryllium copper material die conformal waterway part manufactured by adopting the diffusion welding process can be used for mass production, and the efficient cooling efficiency shortens the forming period as much as possible and prolongs the service life. The economic gain is much greater than with conventional die systems.
It should be further noted that the present invention has a significant effect on heat dissipation of the product molded part during the injection molding process. The invention is characterized in that the die steel is used as a forming part material in the traditional die, the beryllium copper material is used in the invention, the heat dissipation effect of the conventional die steel material conformal waterway part is not better than that of the beryllium copper material conformal waterway part, and the beryllium copper material part can also have the conformal waterway by combining the beryllium copper material with a diffusion welding connection process. The molding time of the injection molding part is shortened, and the economic benefit is remarkably improved. The electric appliances presented in the article can be connected with an external main controller and 220V mains supply, and the main controller can be a conventional known device controlled by a computer and the like.
In the description of the present invention, it should be noted that, unless otherwise explicitly specified or limited, the terms "mounted," "connected," and "connected" are to be construed broadly, e.g., as meaning either a fixed connection, a removable connection, or an integral connection; can be mechanically or electrically connected; they may be connected directly or indirectly through intervening media, or they may be interconnected between two elements. The specific meaning of the above terms in the present invention can be understood by those of ordinary skill in the art through specific situations.
While the preferred embodiments of the present invention have been described in detail, the present invention is not limited to the above embodiments, and various changes can be made without departing from the spirit of the present invention within the knowledge of those skilled in the art. And are neither required nor exhaustive of all embodiments. And obvious variations or modifications of the invention may be made without departing from the scope of the invention.
Claims (10)
1. The mold conformal water channel based on the beryllium copper material is characterized in that the mold conformal water channel based on the beryllium copper material is manufactured by adopting the beryllium copper material, and specifically comprises the following steps:
the pipe body is arranged in the die and used for transmitting a heat transfer medium so as to regulate the temperature of the die, the pipe body is of a multilayer pipeline structure, and adjacent two layers of pipeline structures are connected in a diffusion welding mode to form a communicating structure; and
and the connecting ports are arranged at one end of the pipe body, are a plurality of and are respectively communicated with the corresponding parts of the pipe body in a diffusion welding mode so as to realize the inlet and outlet of the heat transfer medium, and are communicated with the outside of the mould.
2. The beryllium-copper-material-based mold conformal waterway according to claim 1, wherein the mold is made of beryllium copper, and specifically comprises a mold main body, an injection molding glue inlet is formed in the axis of the mold main body, and the injection molding glue inlet is used for injecting materials into the mold for machining and molding.
3. The beryllium copper material-based mold conformal waterway according to claim 1, wherein the mold body is further provided with a plurality of first mounting holes and a plurality of second mounting holes for mounting the tube body.
4. The beryllium-copper-material-based mold conformal waterway according to claim 1, wherein a plurality of waterway inlet and outlet holes are correspondingly formed in an outer wall of one side of the mold body, which is close to the connecting port, and the waterway inlet and outlet holes are communicated with the corresponding connecting port so as to realize inlet and outlet of the heat transfer medium.
5. The method for preparing the beryllium copper material-based mold conformal waterway according to any one of claims 1 to 4, wherein the method for preparing the beryllium copper material-based mold conformal waterway specifically comprises the following steps:
drawing the die by using 3D drawing software to obtain a three-dimensional modeling image, and calculating the three-dimensional modeling image by using finite element analysis software to obtain a 3D drawing file of the beryllium copper material-based die shape-following water channel with optimal cooling efficiency;
the method comprises the steps that a 3D drawing file is manufactured in a layered entity mode through beryllium copper materials to obtain a pipe body and a plurality of connectors, the pipe body is of a multilayer pipeline structure, then two adjacent layers of pipeline structures are connected in a diffusion welding mode to form a communicating structure, and meanwhile the connectors are respectively communicated with corresponding positions of the pipe body in a diffusion welding mode to form an integral structure;
and carrying out shape processing on the integral structure so as to meet the installation and use requirements of the die.
6. The method for preparing the mold conformal waterway based on the beryllium copper material as claimed in claim 5, wherein the overall structure is in any one of a cuboid structure, a cube structure and a cylinder structure.
7. The method for preparing the mold conformal waterway based on the beryllium copper material as claimed in claim 5, wherein the operation steps of the diffusion welding mode are as follows: the method comprises the steps of attaching and heating a plurality of parts to be diffusion welded to 750-810 ℃, then carrying out heat preservation for 3-6 hours, applying pressure of 6-20 MPa to the plurality of parts during the heat preservation, keeping the pressure for 3-6 hours, and cooling.
8. The beryllium copper material-based mold conformal waterway prepared by the method as claimed in any one of claims 5 to 7.
9. Use of a beryllium copper material based mold tracing waterway according to claim 1, 2, 3, 4 or 8 in mold processing.
10. Use of a method for preparing a mold conformal waterway based on beryllium copper material as claimed in any one of claims 5 to 7 in the manufacture of articles made of beryllium copper material.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011007551.2A CN112060423A (en) | 2020-09-23 | 2020-09-23 | Beryllium-copper-material-based mold conformal waterway and preparation method and application thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011007551.2A CN112060423A (en) | 2020-09-23 | 2020-09-23 | Beryllium-copper-material-based mold conformal waterway and preparation method and application thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN112060423A true CN112060423A (en) | 2020-12-11 |
Family
ID=73680834
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202011007551.2A Withdrawn CN112060423A (en) | 2020-09-23 | 2020-09-23 | Beryllium-copper-material-based mold conformal waterway and preparation method and application thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN112060423A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113510451A (en) * | 2021-04-20 | 2021-10-19 | 昆山缔微致精密电子有限公司 | A 3D special-shaped waterway manufacturing process |
| CN115815773A (en) * | 2022-12-15 | 2023-03-21 | 先导薄膜材料有限公司 | Diffusion welding method for beryllium copper and tool steel |
-
2020
- 2020-09-23 CN CN202011007551.2A patent/CN112060423A/en not_active Withdrawn
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113510451A (en) * | 2021-04-20 | 2021-10-19 | 昆山缔微致精密电子有限公司 | A 3D special-shaped waterway manufacturing process |
| CN115815773A (en) * | 2022-12-15 | 2023-03-21 | 先导薄膜材料有限公司 | Diffusion welding method for beryllium copper and tool steel |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103587005A (en) | Maze conformal cooling method and structure of mold | |
| CN101670627A (en) | Mould structure with conformal cooling pipe | |
| CN212860100U (en) | Beryllium-copper-material-based mold conformal water channel | |
| CN1700960A (en) | Method for making a tool for forming a material and tool obtainable by said method | |
| CN111843394A (en) | A grooved ultra-thin aluminum-based soaking plate and preparation method thereof | |
| WO2008008703A2 (en) | Compound tooling for controlled work surface characteristics | |
| CN109249185B (en) | Manufacturing method of water cooling plate | |
| CN207205229U (en) | Die casting and die casting equipment | |
| CN114211714A (en) | Double-helix macro-micro conformal cooling water channel based on selective laser melting | |
| JP3181468U (en) | Heat conduction module | |
| CN212194024U (en) | Injection mold capable of effectively reducing weld lines | |
| CN207219258U (en) | A kind of three-dimensional heat abstractor | |
| WO2021248377A1 (en) | Hydrogen refueling apparatus, cooling apparatus thereof, and manufacturing method for cooling apparatus | |
| CN118322430A (en) | A method for making conformal water channels for efficient uniform cooling optical molds | |
| CN210711262U (en) | 3D glass hot bending forming device | |
| CN212288313U (en) | Shaping mold with good cooling effect | |
| CN113799328B (en) | Injection mold and manufacturing method | |
| CN214188242U (en) | Plastic mold for processing cooling fan | |
| CN209869279U (en) | Metal 3D prints base plate grafting mould | |
| CN211467513U (en) | 3D printer control device | |
| CN204353719U (en) | Mould with shape-following temperature control pipeline | |
| CN219370249U (en) | Multi-pipeline integrated die temperature controller | |
| CN218963987U (en) | Sprue bush structure of die casting die | |
| CN221734784U (en) | A die casting mold core | |
| CN216370103U (en) | Precision mold for rapid molding of high-grade mechanical component |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WW01 | Invention patent application withdrawn after publication |
Application publication date: 20201211 |
|
| WW01 | Invention patent application withdrawn after publication |