CN111929308A - Mobile phone iron frame appearance defect detection system - Google Patents
Mobile phone iron frame appearance defect detection system Download PDFInfo
- Publication number
- CN111929308A CN111929308A CN202010882654.7A CN202010882654A CN111929308A CN 111929308 A CN111929308 A CN 111929308A CN 202010882654 A CN202010882654 A CN 202010882654A CN 111929308 A CN111929308 A CN 111929308A
- Authority
- CN
- China
- Prior art keywords
- station
- inspection
- detection
- defective product
- mobile phone
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01N—INVESTIGATING OR ANALYSING MATERIALS BY DETERMINING THEIR CHEMICAL OR PHYSICAL PROPERTIES
- G01N21/00—Investigating or analysing materials by the use of optical means, i.e. using sub-millimetre waves, infrared, visible or ultraviolet light
- G01N21/84—Systems specially adapted for particular applications
- G01N21/88—Investigating the presence of flaws or contamination
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01N—INVESTIGATING OR ANALYSING MATERIALS BY DETERMINING THEIR CHEMICAL OR PHYSICAL PROPERTIES
- G01N21/00—Investigating or analysing materials by the use of optical means, i.e. using sub-millimetre waves, infrared, visible or ultraviolet light
- G01N21/01—Arrangements or apparatus for facilitating the optical investigation
- G01N21/13—Moving of cuvettes or solid samples to or from the investigating station
Landscapes
- Physics & Mathematics (AREA)
- Health & Medical Sciences (AREA)
- Life Sciences & Earth Sciences (AREA)
- Chemical & Material Sciences (AREA)
- Analytical Chemistry (AREA)
- Biochemistry (AREA)
- General Health & Medical Sciences (AREA)
- General Physics & Mathematics (AREA)
- Immunology (AREA)
- Pathology (AREA)
- Investigating Materials By The Use Of Optical Means Adapted For Particular Applications (AREA)
Abstract
本发明公开了一种手机铁框外观缺陷检测系统,包括检测台、送检流水线和良品流水线,以及送检机械手和良品机械手,检测台上设有第一检测工位、第二检测工位和良品取料工位,第二检测工位和良品取料工位之间设有第三检测工位和次品取料工位;第一检测工位和第二检测工位分别设有CCD视觉组件A和CCD视觉组件B,第三检测工位设有CCD线扫描视觉检测组件;检测台上以可转动方式设置有四工位分度盘,四工位分度盘上具有四个治具,四工位分度盘转动,能够使各治具依次在第二检测工位、第三检测工位、良品取料工位和次品取料工位之间切换。满足手机铁框外观缺陷检测指标需求,实现在线快速检测,提高检测效率和质量,系统可靠性和稳定性极好。
The invention discloses an appearance defect detection system of a mobile phone iron frame. The good product reclaiming station, the third inspection station and the defective product reclaiming station are arranged between the second inspection station and the good product reclaiming station; the first inspection station and the second inspection station are respectively equipped with CCD vision Component A and CCD vision component B, the third detection station is equipped with a CCD line scanning visual detection component; a four-station indexing plate is rotatably set on the inspection table, and there are four fixtures on the four-station indexing plate , The rotation of the four-station indexing plate can make each jig switch between the second inspection station, the third inspection station, the good product reclaiming station and the defective product reclaiming station in turn. It can meet the requirements of mobile phone iron frame appearance defect detection indicators, realize online rapid detection, improve detection efficiency and quality, and system reliability and stability are excellent.
Description
技术领域technical field
本发明涉及手机零部件检测技术领域,具体涉及一种手机铁框外观缺陷检测系统。The invention relates to the technical field of mobile phone parts detection, in particular to a mobile phone iron frame appearance defect detection system.
背景技术Background technique
铁框是手机背光模组的重要部件之一,通常需要在铁框上对应摄像头位置进行开孔,而孔的质量缺陷会对使用视觉效果产生直接影响,降低用户体验感,此外,铁框表面平整度也直接影响了手机其他部件的安装效果,而冲压过程中铁框表面也容易变形产生凹凸点,故在生产过程中,必须对铁框上的通孔及铁框表面进行检测,以防止次品进入总装线。The iron frame is one of the important parts of the backlight module of the mobile phone. It is usually necessary to make holes on the iron frame corresponding to the camera position. The quality defects of the holes will directly affect the visual effect and reduce the user experience. In addition, the surface of the iron frame The flatness also directly affects the installation effect of other parts of the mobile phone, and the surface of the iron frame is easily deformed during the stamping process to produce bumps. Therefore, in the production process, the through holes on the iron frame and the surface of the iron frame must be tested to prevent secondary The product enters the final assembly line.
现有技术中,大多采用人工抽样检测的方式,其检测效率低,可靠性较差,另外由于铁框上的通孔是冲压而成,冲压后翻边部分在铁框表面形成一个凸起圆环,圆环边缘是否开裂变形,或者通孔根部是否破裂产生小孔,以及铁框表面是否有凹凸点或脏污,这些都是需要检测的指标,导致很难利用现有的一些视觉检测设备来检测,故亟需一种能够快速检测手机铁框质量的设备,能够完成外观检测指标,同时提高检测效率和可靠性,满足自动化的生产需求。In the prior art, manual sampling detection is mostly used, which has low detection efficiency and poor reliability. In addition, since the through holes on the iron frame are punched, the flanging part after punching forms a raised circle on the surface of the iron frame. Whether the edge of the ring or the ring is cracked and deformed, or whether the root of the through hole is cracked to produce small holes, and whether there are bumps or dirt on the surface of the iron frame, these are the indicators that need to be detected, which makes it difficult to use some existing visual inspection equipment. Therefore, there is an urgent need for a device that can quickly detect the quality of the iron frame of the mobile phone, which can complete the appearance detection index, and at the same time improve the detection efficiency and reliability, and meet the needs of automated production.
发明内容SUMMARY OF THE INVENTION
为解决上述问题,本发明提供了一种手机铁框外观缺陷检测系统,能够实现手机铁框外观质量快速检测,提高检测效率。In order to solve the above problems, the present invention provides a system for detecting the appearance defects of the iron frame of the mobile phone, which can realize the rapid detection of the appearance quality of the iron frame of the mobile phone and improve the detection efficiency.
为实现上述目的,本发明技术方案如下:For achieving the above object, the technical scheme of the present invention is as follows:
一种手机铁框外观缺陷检测系统,其关键在于:包括检测台,以及对应该检测台设置的送检流水线和良品流水线,所述检测台上具有与送检流水线和良品流水线一一对应的送检机械手和良品机械手,其中检测台上对应送检机械手的位置设有第一检测工位和第二检测工位,对应良品机械手设有良品取料工位,所述第二检测工位和良品取料工位之间设有第三检测工位和次品取料工位;A mobile phone iron frame appearance defect detection system, the key of which is that it includes a detection table, and a delivery line and a good product line set corresponding to the detection table, and the detection table has a one-to-one correspondence with the delivery line and the good product line. Inspection manipulator and good product manipulator, wherein the position corresponding to the inspection manipulator on the inspection table is provided with a first inspection station and a second inspection station, and the corresponding good product manipulator is provided with a good product reclaiming station, the second inspection station and the good product There is a third inspection station and a defective reclaiming station between the reclaiming stations;
所述第一检测工位和第二检测工位分别设有CCD视觉组件A和CCD视觉组件B,第三检测工位设有CCD线扫描视觉检测组件;The first detection station and the second detection station are respectively provided with a CCD visual component A and a CCD visual component B, and the third detection station is provided with a CCD line scan visual detection component;
所述检测台上以可转动方式设置有四工位分度盘,所述四工位分度盘上具有四个治具,所述四工位分度盘转动,能够使各治具依次在第二检测工位、第三检测工位、良品取料工位和次品取料工位之间切换。A four-station indexing plate is rotatably arranged on the inspection table, and the four-station indexing plate has four jigs. Switch between the second inspection station, the third inspection station, the good product reclaiming station and the defective product reclaiming station.
采用以上方案,主要通过在三个检测工位完成手机铁框的外观缺陷检测,有针对性的通过CCD视觉组件A检测孔内侧裂情况,CCD视觉组件B则用来检测冲压通孔圆环边缘外观质量,CCD线扫描视觉检测组件来检测铁框外表面凹凸情况,满足铁框三项外观检测需求,并通过四工位分度盘,实现在线检测,大大提高检测效率和可靠性。Using the above scheme, the appearance defect detection of the iron frame of the mobile phone is mainly completed in three inspection stations. The CCD vision component A is used to detect the inner crack of the hole, and the CCD vision component B is used to detect the edge of the punched through-hole ring. Appearance quality, CCD line scanning visual inspection component to detect the concavity and convexity of the outer surface of the iron frame, to meet the three appearance inspection requirements of the iron frame, and through the four-station indexing plate, online inspection is realized, which greatly improves the inspection efficiency and reliability.
作为优选:所述送检流水线和良品流水线分别位于检测台的正对两侧,所述第二检测工位、第三检测工位、良品取料工位和次品取料工位依次呈圆周阵列分布。采用以上布置方式,有利于提高系统整体紧凑性,将良品取料工位紧邻第三检测工位设置,有利于提高运转效率。Preferably: the inspection-submission line and the good-quality production line are located on the opposite sides of the detection table, respectively, and the second detection station, the third detection station, the good-quality reclaiming station and the defective-reclaiming station are in a circle in sequence. array distribution. The above arrangement is beneficial to improve the overall compactness of the system, and the good product reclaiming station is arranged next to the third detection station, which is beneficial to improve the operation efficiency.
作为优选:所述CCD线扫描视觉检测组件包括位于检测台上方的线扫描相机和线扫描光源;Preferably: the CCD line scan visual inspection component includes a line scan camera and a line scan light source located above the detection stage;
四个所述治具在四工位分度盘上呈圆周阵列分布,并与所述四工位分度盘滑动配合,所述检测台上对应第三检测工位设有直线驱动机构,所述治具能够在直线驱动机构的驱动下沿检测台直线移动,其移动距离至少大于待检铁框的宽度。采用以上方案,通过直线驱动机构推动治具移动,即使线扫描相机能够完成对铁框表面的全部扫描,相对提高检测质量,且能够根据需要调整直线机构移动行程距离,以适应不同尺寸铁框。The four jigs are distributed in a circular array on the four-station indexing plate, and are slidably matched with the four-station indexing plate. The inspection table is provided with a linear drive mechanism corresponding to the third inspection station. The jig can move linearly along the inspection table under the drive of the linear drive mechanism, and the moving distance is at least greater than the width of the iron frame to be inspected. With the above solution, the jig is moved by the linear drive mechanism, even if the line scan camera can complete all the scans on the surface of the iron frame, the inspection quality is relatively improved, and the travel distance of the linear mechanism can be adjusted as needed to adapt to different sizes of iron frames.
作为优选:所述直线驱动机构包括正对四工位分度盘中心设置的推杆,以及用于驱动推杆直线移动的丝杆电机,所述四工位分度盘的中部设有安装座,各治具与该安装座之间均设有弹性复位结构。采用以上方案,以丝杆电机驱动推杆前移,有利于保证其顶推稳定性,通过弹性复位结构可使完成扫描之后的治具复位,而不会对其他工位的操作造成影响。Preferably: the linear drive mechanism includes a push rod facing the center of the four-station indexing plate, and a screw motor for driving the push rod to move linearly, and a mounting seat is provided in the middle of the four-station indexing plate , an elastic reset structure is arranged between each fixture and the mounting seat. Using the above scheme, the screw motor drives the push rod to move forward, which is beneficial to ensure the stability of the push rod. The elastic reset structure can reset the fixture after scanning, without affecting the operation of other stations.
作为优选:所述治具均为真空吸附式治具,四工位分度盘的中部设有旋转供气头。采用以上方案,有利于保证铁框在治具上的稳定性,防止分度盘旋转将铁框甩出,同时减少铁框的相对振动,有利于提高检测效果。Preferably, the fixtures are all vacuum adsorption fixtures, and a rotary air supply head is arranged in the middle of the four-station indexing plate. Adopting the above scheme is beneficial to ensure the stability of the iron frame on the fixture, prevent the indexing plate from rotating and throw the iron frame out, and at the same time reduce the relative vibration of the iron frame, which is beneficial to improve the detection effect.
作为优选:所述送检流水线、第一检测工位和第二检测工位依次呈九十度夹角分布,所述送检机械手包括以可转动方式安装在检测台上的悬臂支架、以及用于驱动该悬臂支架水平转动的伺服马达A,所述悬臂支架上具有两个水平设置并呈正交分布的吸盘A,各吸盘A均配置有滑台气缸,所述滑台气缸竖直朝下。送检流水线、第一检测工位和第二检测工位采用以上分布方式,配合送检机械手结构,有利于提高检测效率,减少等待时间等。Preferably, the inspection line, the first inspection station and the second inspection station are distributed at an angle of 90 degrees in sequence, and the inspection manipulator includes a cantilever bracket rotatably installed on the inspection table, and a For the servo motor A that drives the cantilever support to rotate horizontally, the cantilever support has two horizontally arranged and orthogonally distributed suction cups A, each suction cup A is equipped with a sliding table cylinder, and the sliding table cylinder is vertically downward. . The inspection line, the first inspection station and the second inspection station adopt the above distribution methods, and cooperate with the inspection robot structure, which is beneficial to improve the inspection efficiency and reduce the waiting time.
作为优选:所述第一检测工位设有放置台,所述CCD视觉组件A包括分别位于放置台上下两侧的面阵相机A和面光源,所述面阵相机A和面光源倾斜设置,其中面阵相机A配置有镜头,面光源靠近放置台的一端端部。采用以上方案,有利于提高对孔内侧裂情况的检测,且不妨碍正常取放料。Preferably: the first detection station is provided with a placing table, the CCD vision assembly A includes an area array camera A and a surface light source located on the upper and lower sides of the placing table, respectively, and the area array camera A and the surface light source are arranged obliquely, The area scan camera A is equipped with a lens, and the area light source is close to one end of the placing table. Adopting the above scheme is beneficial to improve the detection of cracks inside the hole, and does not hinder the normal taking and unloading of materials.
作为优选:所述CCD视觉组件B包括环形光源和面阵相机B,所述环形光源和面阵相机B依次设于四工位分度盘下方,所述面阵相机B竖直朝上。采用以上方案,有利于减少检测台上方空间占用,在不妨碍分度盘正常转动前提下,配合环形光源,提高对冲压通孔圆环边缘外观检测质量。Preferably, the CCD vision assembly B includes a ring light source and an area scan camera B, the ring light source and the area scan camera B are sequentially arranged below the four-station indexing plate, and the area scan camera B is vertically upward. The adoption of the above scheme is beneficial to reduce the space occupation above the inspection table, and on the premise of not hindering the normal rotation of the indexing plate, the annular light source is used to improve the appearance inspection quality of the edge of the punched through-hole ring.
作为优选:所述送检流水线远离检测台的一端配置有上料单元,所述上料单元包括上料台,以可转动方式安装在该上料台上的上料转盘,以及用于驱动所述上料转盘转动的伺服马达B;Preferably, a feeding unit is arranged at one end of the inspection line away from the inspection table, and the feeding unit includes a feeding table, a feeding turntable rotatably mounted on the feeding table, and a feeding turntable for driving the feeding table. The servo motor B that rotates the feeding turntable;
所述上料台靠近送检流水线的位置设有上料机械手,所述上料转盘上设有至少两个顶部敞口的料仓,所述料仓底部具有顶升口,上料台底部对应上料机械手设有顶升上料机构。The loading table is provided with a loading manipulator at a position close to the inspection line, the loading turntable is provided with at least two silos with open tops, and the bottom of the silos has a lifting opening, and the bottom of the loading table corresponds to The feeding manipulator is provided with a lifting and feeding mechanism.
采用以上方案,使用时将多个待检铁框放置在料仓内,利用上料机械手将其依次抓取并放置到送检流水线上,而顶升上料机构则可对料仓内的铁框进行实时顶升,确保最上面的铁框始终处于固定高度,以便上料机械手抓取,而一个料仓内的铁框抓取检测完之后,亦可伺服马达B驱动上料转盘转动,使下一个料仓对应上料机械手的抓取位置,而员工或机械则可对空出的料仓进行补充,有利于提高检测效率,满足大批量检测需求。Using the above scheme, when using, place multiple iron frames to be inspected in the silo, and use the feeding manipulator to grab them in turn and place them on the inspection line. The frame is lifted in real time to ensure that the top iron frame is always at a fixed height, so that the feeding manipulator can grab it. The next silo corresponds to the grabbing position of the feeding manipulator, and employees or machinery can supplement the emptied silo, which is beneficial to improve the inspection efficiency and meet the needs of large-scale inspection.
作为优选:所述次品取料工位设有次品机械手,所述上料机械手、良品机械手和次品机械手均为180°旋转双吸盘机械手。采用以上方案,有利于提高各工位操作效率,且制造成本低,便于实施等。Preferably, the defective product reclaiming station is provided with a defective product manipulator, and the feeding manipulator, the good product manipulator and the defective product manipulator are all 180° rotating double suction cup manipulators. The adoption of the above scheme is beneficial to improve the operation efficiency of each station, and the manufacturing cost is low, and the implementation is convenient.
与现有技术相比,本发明的有益效果是:Compared with the prior art, the beneficial effects of the present invention are:
采用本发明提供的手机铁框外观缺陷检测系统,满足手机铁框外观缺陷检测指标需求,并能够实现在线快速检测,提高检测效率和质量,系统可靠性和稳定性极好。The application of the mobile phone iron frame appearance defect detection system provided by the invention can meet the requirements of the mobile phone iron frame appearance defect detection index, and can realize online rapid detection, improve the detection efficiency and quality, and the system reliability and stability are excellent.
附图说明Description of drawings
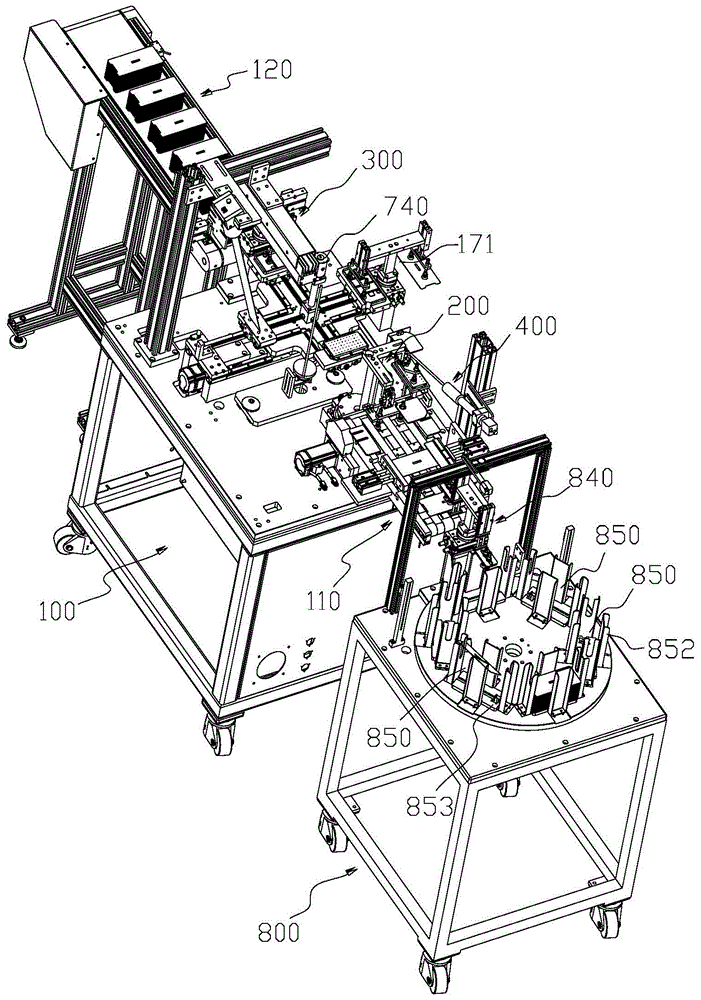
图1为本发明的结构示意图;Fig. 1 is the structural representation of the present invention;
图2为本发明的侧视图;Fig. 2 is the side view of the present invention;
图3为本发明的俯视图;Fig. 3 is the top view of the present invention;
图4为上料转盘的结构示意图;Fig. 4 is the structural representation of the feeding turntable;
图5为顶升上料机构的结构示意图;Figure 5 is a schematic structural diagram of a jacking and feeding mechanism;
图6为送检流水线的结构示意图;Fig. 6 is the structural representation of the inspection pipeline;
图7为送检机械手的结构示意图;Fig. 7 is the structural representation of the inspection robot;
图8为CCD视觉组件A结构示意图;FIG. 8 is a schematic structural diagram of the CCD vision assembly A;
图9为CCD视觉组件B的结构示意图;Fig. 9 is the structural representation of CCD vision assembly B;
图10为CCD线扫描视觉检测组件与四工位分度盘安装结构示意图;Figure 10 is a schematic diagram of the installation structure of the CCD line scanning visual inspection component and the four-station indexing plate;
图11为直线驱动机构的结构示意图。FIG. 11 is a schematic structural diagram of a linear drive mechanism.
具体实施方式Detailed ways
以下结合实施例和附图对本发明作进一步说明。The present invention will be further described below with reference to the embodiments and the accompanying drawings.
参考图1和图11所示的手机铁框外观缺陷检测系统,其主要包括检测台100,以及对应该检测台100设置的送检流水线110和良品流水线120,检测台100对应送检流水线110和良品流水线120的分别设有送检机械手200和良品机械手300,与此同时,检测台100上对应送检机械手200的位置设有第一检测工位130和第二检测工位140,对应良品机械手300设有良品取料工位150,第二检测工位140和良品取料工位150之间设有第三检测工位160和次品取料工位170。Referring to the appearance defect detection system of the mobile phone iron frame shown in FIG. 1 and FIG. 11 , it mainly includes an
第一检测工位130和第二检测工位140分别设有CCD视觉组件A400和CCD视觉组件B500,第三检测工位160设有CCD线扫描视觉检测组件600,其中CCD视觉组件A400用于检测通孔内侧的侧裂情况,CCD视觉组件B500用于检测铁框上冲压通孔圆环边缘的外观质量,而CCD线扫描视觉检测组件600主要以线扫描形式完成对铁框表面凹凸情况的检测。The
送检机械手200主要用于将送检流水线110上的待检铁框抓取放到第一检测工位130,完成一次检测,并将第一检测工位130完成检测的一次检测的铁框抓取放到第二检测工位,良品机械手300用于将处于良品取料工位150内,且质量合格的铁框抓取放到良品流水线120,质量不符的铁框则被转运到次品取料工位170,被单独处理。The
为提高检测效率,减少设备运转空行程及结构复杂度等,本申请的检测台100上以可转动方式设置有四工位分度盘700,如图所示,四工位分度盘700上具有四个治具710,当四工位分度盘700转动时,能够使各治具710依次在第二检测工位140、第三检测工位160、良品取料工位150和次品取料工位170之间切换,即四工位分度盘700每一次转动,带动治具710移动一个工位的距离,使其与下一工位对正,以便进行相应工位操作。In order to improve the detection efficiency, reduce the idle travel of the equipment and the structural complexity, etc., the detection table 100 of the present application is provided with a four-
参考图3,本实施例中送检流水线110和良品流水线120分别位于检测台100的左右两侧,第二检测工位140、第三检测工位160、良品取料工位150和次品取料工位170依次呈圆周阵列分布,即相邻两个工位之间夹角为90°,治具710与其分布圆周的切线相互平行,而送检流水线110、第一检测工位130和第二检测工位140之间也依次呈90°夹角分布,其中第二检测工位140与送检流水线110正对设置,第一检测工位130位于二者的同一侧。Referring to FIG. 3 , in this embodiment, the
在此基础之上,结合图7,本实施例中的送检机械手200主要包括以可转动方式安装在检测台100上的悬臂支架210,悬臂支架210竖向设置,检测台100上配置有用于驱动悬臂支架210水平转动的伺服马达A211,悬臂支架210的顶部具有两个相互垂直且一体成型的悬臂214,各悬臂214上通过滑台气缸213连接安装有一个吸盘A212,如图所示,滑台气缸213均竖直朝下,吸盘A212水平设置,吸盘A212沿各自悬臂214的宽度方向设置,故两个悬臂214上的吸盘A212相互垂直,吸盘A212为真空吸盘式结构,有另外配置的气源即气控系统,送检机械手200工作时,当其中一个吸盘A212位于送检流水线110上方时,另外一个吸盘A212则位于第一检测工位130的上方,而转动90°之后,两个吸盘A212则分别位于第一检测工位130和第二检测工位140上方,操作过程中,通过两个吸盘A212对待检铁框的一吸一放,大大提高了检测效率。On this basis, with reference to FIG. 7 , the
再结合图8和图9,本实施例中尽量采用模块化的安装结构,以提高系统的装配性和维修性,如图所示,第一检测工位130处于具有以可拆卸方式设置的基板A132,该基板A132大体呈Z形,其两端分别设有前立架133和后立架134,两个立架在宽度方向错开一定距离,其中前立架133的顶部具有水平设置的放置台131,检测时,送检机械手200将送检流水线110上的待检铁框抓取放置到该放置台131上以进行第一次检测。8 and 9 again, in this embodiment, a modular installation structure is adopted as much as possible to improve the assembly and maintainability of the system. As shown in the figure, the
CCD视觉组件A400包括分别位于放置台131上下两侧的面阵相机A410和面光源420,面阵相机A410和面光源420倾斜设置,其中面阵相机A410配置有镜头430,面光源420靠近放置台131的一端端部,如图所示,面阵相机A410以倾斜向下的方式固设在后立架134上,而面光源420则通过L形支架135固设在前立架133,这样在进行第一检测工位130的组装时,只需在基板A132上完成放置台131,以及CCD视觉组件A400安装,然后整体固定到检测台100上,并进行线路连接即可,有利于提高系统组装效率。The CCD vision assembly A400 includes an area scan camera A410 and a
同理,CCD视觉组件B500主要包括基板B530,以及安装在该基板B530上的环形光源510和面阵相机B520,如图所示,CCD视觉组件B500整体位于四工位分度盘700下方,并优选环形光源510为碗灯,通过上立板540固定支撑在基板B530的上方,面阵相机B510通过下立板550固设于基板B530的下方,并竖直朝上,与环形光源510同轴设置,基板B530上正对面阵相机B510的位置开设有过孔531,在进行第二检测工位140的构建时,只需将基板B530固设在检测台100上,并对管线进行连接即可。Similarly, the CCD vision assembly B500 mainly includes a substrate B530, a ring
参考图1至图3,图10和图11,本申请中CCD线扫描视觉检测组件600主要包括位于检测台100上方的线扫描相机610和线扫描光源620,如图所示,CCD线扫描视觉检测组件600通过立柱630安装在检测台100上方,线扫描光源620为灯板结构,以减少暗影区域,并位于第三检测工位160的正上方,线扫描相机610倾斜向下设置。1 to 3, 10 and 11, the CCD line scan
第三检测工位160主要是用于完成对待检铁框的表面凹凸情况进行检测,故在采用线扫描方式检测时,检测过程中,需要扫描线与待检铁框之间能够发生相对移动,以确保完成整个表面扫描,而如果移动CCD线扫描视觉检测组件600,则大大增加其振动频率,降低了检测质量,故本申请中优选移动待检铁框的方式,如图所示,四个治具710在四工位分度盘700上呈圆周阵列分布,并与所述四工位分度盘700滑动配合,检测台100上对应第三检测工位160设有直线驱动机构720,治具710能够在直线驱动机构720的驱动下直线移动,其移动距离至少大于待检铁框的宽度,如果线扫描相机610的设定扫面线位于治具710的外侧,则直线驱动机构720用于驱动治具710朝外移动,使其上放置的待检铁框能够全部通过扫面线,反之,当扫面线位于治具710的内侧,则直线驱动机构720用于驱动治具710朝内移动。The
其具体结构如图所示,本实施例中四工位分度盘700大体呈对称的十字叉结构,检测台100底部设有用于驱动四工位分度盘700转动的伺服马达C,四工位分度盘700上对应每个治具710均具有对称设置的两个导轨A770,导轨A770沿四工位分度盘700转动圆周的径向设置,治具710与对应的导轨A770滑动配合,四工位分度盘700的中部设有安装座730,安装座730对应每个治具710设有导杆750,治具710活套在对应的导杆750上,与此同时,导杆750上套设有复位弹簧760,复位弹簧760位于治具710与该安装座730之间,导杆750的末端固设有止挡头751。Its specific structure is shown in the figure. In this embodiment, the four-
相应的,本实施例中的直线驱动机构720包括正对四工位分度盘700中心设置的推杆721,以及用于驱动推杆721直线移动的丝杆电机722,如图所示,丝杆电机722水平朝内设置,其丝杆正对四工位分度盘700的转动中心,并配置有与其匹配的螺母座723,丝杆电机722左右两侧具有对称设置的侧板724,侧板724顶部具有与导轨A770平行设置的导轨B725,导轨B725上具有与其滑动配合的推动块726,推动块726与螺母座723固定连接,推杆721固设于推动块726上,并正对治具710延伸,检测时,丝杆电机722工作,推动推杆721平稳前移,推杆721推动正对的治具710向内滑动,完成整个表面扫描,复位弹簧760始终处于压缩状态,扫描完成之后,丝杆电机722反转,推杆721回退到初始位置,而治具710则在复位弹簧760的作用下快速复位。Correspondingly, the
为防止四工位分度盘700转动以及治具710移动过程中,其上放置的铁框错位或脱落等,故本实施例中优选治具710为真空吸附式治具,相应的在四工位分度盘700中部安装座730上具有以可转动方式设置的旋转供气头740,其主要用于实现对各治具710抽放真空的单独控制,防止管线缠绕,提高其可行性等。In order to prevent the iron frame placed on it from being dislocated or falling off during the rotation of the four-
参考图1至图6,本申请的检测系统还配置有上料单元800,上料单元800靠近送检流水线110远离检测台100的一端,如图所示,上料单元800主要包括上料台810,以可转动方式安装在该上料台810上的上料转盘820,以及用于驱动上料转盘820转动的伺服马达B830,且上料转盘820和伺服马达B830分别位于上料台810的上下两侧。Referring to FIG. 1 to FIG. 6 , the detection system of the present application is further configured with a
上料台810上靠近送检流水线110的位置设有上料机械手840,上料转盘820上设有至少两个顶部敞口的料仓850,料仓850沿上料转盘820的圆周均匀分布,料仓850底部具有顶升口851,上料台810底部对应上料机械手840设有顶升上料机构860,上料机械手840用于将对应料仓850内的待检铁框抓取放置到送检流水线110上。A
料仓850由四个挡板852合围而成,其底部具有活动设置的底板853,底板853与正对的挡板852具有滑动配合结构,底板853能够完全覆盖顶升口851,顶升上料机构860主要包括水平设置的推板862,以及用于驱动推板862竖直升降的伺服马达D861,其中推板862大小与顶升口851相适应,其能够在伺服马达D861驱动下通过顶升口851伸入料仓850中,并推动底板853上移,以调整放入铁框的高度,确保最上层铁框始终处于设定高度位置,以便机械手抓取。The
本实施例中,次品取料工位170设有次品机械手171,其当铁框检测不合格时,则随四工位分度盘700转动至次品取料工位170,再经由次品机械手171抓取放置到废品收纳箱中,如图1至图3所示,上料机械手840、良品机械手300和次品机械手171均为180°旋转双吸盘机械手,具有两个正对且水平设置的吸盘B,均能够实现一吸一放同步操作,以提高对应工位操作效率。In this embodiment, the defective
参考图6,送检流水线110主要由两个正对设置的滚筒115,以及套设在两个滚筒115上的输送皮带构成,滚筒115配置有伺服马达E114,送检流水线110沿其长度方向依次具有放料工位111、整形工位112和取料工位113,其中放料工位111靠近上料单元800,放料工位111和取料工位113两侧均设有限位块,送检流水线110上对应整形工位112的两侧具有正对设置的整形气缸116,整形气缸116连接有调整块,当待检铁框随输送皮带传送到整形工位112时,整形气缸116推动调整块向内正对移动,能够调整铁框摆正,使其到达取料工位113时的姿态保持一致性。Referring to FIG. 6 , the
参考图1至图11所示的手机铁框外观缺陷检测系统,其工作过程如下:首先将多个待检铁框放入料仓850内,并确保其中一个料仓850位于上料机械手840的一个吸盘B的正下方,上料机械手840抓取料仓850内的待检铁框放到送检流水线110的放料工位111,待检铁框经过整形工位112后到达取料工位113,为送检机械手200抓取。Referring to the appearance defect detection system of the mobile phone iron frame shown in FIG. 1 to FIG. 11 , the working process is as follows: first, put a plurality of iron frames to be inspected into the
送检机械手200转动90°之后,将其放至放置台131上,在此处通过CCD视觉组件A400完成第一次检测,需要注意的是,放置台131的位置与CCD视觉组件A400的相对位置设计,需满足面阵相机A410能够刚好进行待检铁框上通孔部位的扫描,完成第一次检测之后,仍然通过送检机械手200将其抓取并转动90°后,放置到刚好处于第二检测工位140的治具710上,此处需要注意的是,如图2所示,待检铁框在治具710上,其具有通孔的一端突出于治具710的端部,即确保通孔暴露在下方面阵相机B520的扫描范围之内,并完成第二次检测。After the
四工位分度盘700旋转,将完成第二次检测的待检铁框移动到第三检测工位160,在直线驱动机构720作用下完成直线移动,同时受CCD线扫描检测组件600的扫描检测,即完成第三次扫描检测,三个检测工位的检测结果统一传送到后台处理系统,如果判断已检铁框为良品,则当四工位分度盘700转动,使该已检铁框处于良品取料工位170时,则可通过良品机械手150抓取放置到良品流水线120上,反之,若为次品时,则依次转动至其处于次品取料工位170时,则由次品机械手171将其抓取并放入相应的收纳装置中。The four-
最后需要说明的是,上述描述仅仅为本发明的优选实施例,本领域的普通技术人员在本发明的启示下,在不违背本发明宗旨及权利要求的前提下,可以做出多种类似的表示,这样的变换均落入本发明的保护范围之内。Finally, it should be noted that the above description is only a preferred embodiment of the present invention, and those of ordinary skill in the art can make a variety of similar It is indicated that such transformations fall within the protection scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010882654.7A CN111929308A (en) | 2020-08-28 | 2020-08-28 | Mobile phone iron frame appearance defect detection system |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010882654.7A CN111929308A (en) | 2020-08-28 | 2020-08-28 | Mobile phone iron frame appearance defect detection system |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111929308A true CN111929308A (en) | 2020-11-13 |
Family
ID=73309064
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010882654.7A Pending CN111929308A (en) | 2020-08-28 | 2020-08-28 | Mobile phone iron frame appearance defect detection system |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111929308A (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112707175A (en) * | 2021-01-29 | 2021-04-27 | 常熟市龙腾滚动体制造有限公司 | End plate detection and stacking integrated discharging system |
| CN113848212A (en) * | 2021-10-25 | 2021-12-28 | 东莞市长智光视觉科技有限公司 | Inner cavity visual inspection machine and inner cavity detection method |
| CN114705685A (en) * | 2022-01-30 | 2022-07-05 | 中信云网有限公司 | AI visual detection method and system based on deep learning and readable storage medium |
| CN116973306A (en) * | 2023-04-24 | 2023-10-31 | 英业达(重庆)有限公司 | An appearance inspection device |
Citations (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN201575797U (en) * | 2009-06-10 | 2010-09-08 | 上海微曦自动控制技术有限公司 | Pipe-to-pipe visual detection device |
| CN203236466U (en) * | 2012-07-09 | 2013-10-16 | 上海瓦科自动化设备有限公司 | Circular stock bin |
| CN105382650A (en) * | 2015-12-19 | 2016-03-09 | 湖南宇环智能装备有限公司 | Full-automatic double-end-face grinding production line |
| WO2016086333A1 (en) * | 2014-12-01 | 2016-06-09 | 李相鹏 | Visual detection device for screw detection |
| CN105689899A (en) * | 2016-03-25 | 2016-06-22 | 东莞市盛雄激光设备有限公司 | Fully-automatic laser cutting production workstation |
| CN105758307A (en) * | 2016-03-03 | 2016-07-13 | 南京力聚精密锻造有限公司 | Forging part detection device and method |
| CN205522025U (en) * | 2016-03-25 | 2016-08-31 | 东莞市盛雄激光设备有限公司 | Automatic unloading sorting machine |
| CN106053482A (en) * | 2016-06-27 | 2016-10-26 | 宾兴 | Automatic product GAP and STEP detection production line and detection process |
| KR101697119B1 (en) * | 2016-07-07 | 2017-01-18 | 에스에스오트론 주식회사 | apparatus for vision inspection of semiconductor |
| CN106895961A (en) * | 2016-07-29 | 2017-06-27 | 深圳市德仓科技有限公司 | The testing equipment and its detection method of a kind of backlight module |
| CN107262380A (en) * | 2017-07-18 | 2017-10-20 | 深圳中天云创科技有限公司 | A kind of cell phone back light source vision automatic checkout equipment and detection method |
| CN107350872A (en) * | 2017-07-28 | 2017-11-17 | 陕西海力特精密机械有限公司 | Multiple-station rotation lifting combination feeding storage arrangement |
| CN208654049U (en) * | 2018-08-18 | 2019-03-26 | 东莞市鼎星电子科技有限公司 | A device for detecting contour defects of mobile phone casings |
| CN208818648U (en) * | 2018-08-28 | 2019-05-03 | 东莞科卓机器人有限公司 | A kind of line sweeps formula AOI detection device |
| CN209239460U (en) * | 2018-09-19 | 2019-08-13 | 宏利科技(苏州)有限公司 | The intelligent package system of purification filtering cup seal member |
| CN110640028A (en) * | 2018-06-26 | 2020-01-03 | 北京长征火箭装备科技有限公司 | Automatic feeding riveting device and riveting method thereof |
| CN210148558U (en) * | 2019-03-25 | 2020-03-17 | 常州常华光电塑胶有限公司 | Automatic rotary feeding device for plastic spool inserts |
| CN110977080A (en) * | 2019-12-27 | 2020-04-10 | 昆山华誉自动化科技有限公司 | Full-automatic annular PCB board and FPC soft board welding system |
| CN210308876U (en) * | 2019-06-21 | 2020-04-14 | 东莞市本润机器人科技股份有限公司 | Injection molding AOI check out test set |
| CN212433003U (en) * | 2020-08-28 | 2021-01-29 | 雷澳视觉科技(东莞)有限公司 | Automatic detection device for appearance defects of mobile phone iron frame |
-
2020
- 2020-08-28 CN CN202010882654.7A patent/CN111929308A/en active Pending
Patent Citations (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN201575797U (en) * | 2009-06-10 | 2010-09-08 | 上海微曦自动控制技术有限公司 | Pipe-to-pipe visual detection device |
| CN203236466U (en) * | 2012-07-09 | 2013-10-16 | 上海瓦科自动化设备有限公司 | Circular stock bin |
| WO2016086333A1 (en) * | 2014-12-01 | 2016-06-09 | 李相鹏 | Visual detection device for screw detection |
| CN105382650A (en) * | 2015-12-19 | 2016-03-09 | 湖南宇环智能装备有限公司 | Full-automatic double-end-face grinding production line |
| CN105758307A (en) * | 2016-03-03 | 2016-07-13 | 南京力聚精密锻造有限公司 | Forging part detection device and method |
| CN105689899A (en) * | 2016-03-25 | 2016-06-22 | 东莞市盛雄激光设备有限公司 | Fully-automatic laser cutting production workstation |
| CN205522025U (en) * | 2016-03-25 | 2016-08-31 | 东莞市盛雄激光设备有限公司 | Automatic unloading sorting machine |
| CN106053482A (en) * | 2016-06-27 | 2016-10-26 | 宾兴 | Automatic product GAP and STEP detection production line and detection process |
| KR101697119B1 (en) * | 2016-07-07 | 2017-01-18 | 에스에스오트론 주식회사 | apparatus for vision inspection of semiconductor |
| CN106895961A (en) * | 2016-07-29 | 2017-06-27 | 深圳市德仓科技有限公司 | The testing equipment and its detection method of a kind of backlight module |
| CN107262380A (en) * | 2017-07-18 | 2017-10-20 | 深圳中天云创科技有限公司 | A kind of cell phone back light source vision automatic checkout equipment and detection method |
| CN107350872A (en) * | 2017-07-28 | 2017-11-17 | 陕西海力特精密机械有限公司 | Multiple-station rotation lifting combination feeding storage arrangement |
| CN110640028A (en) * | 2018-06-26 | 2020-01-03 | 北京长征火箭装备科技有限公司 | Automatic feeding riveting device and riveting method thereof |
| CN208654049U (en) * | 2018-08-18 | 2019-03-26 | 东莞市鼎星电子科技有限公司 | A device for detecting contour defects of mobile phone casings |
| CN208818648U (en) * | 2018-08-28 | 2019-05-03 | 东莞科卓机器人有限公司 | A kind of line sweeps formula AOI detection device |
| CN209239460U (en) * | 2018-09-19 | 2019-08-13 | 宏利科技(苏州)有限公司 | The intelligent package system of purification filtering cup seal member |
| CN210148558U (en) * | 2019-03-25 | 2020-03-17 | 常州常华光电塑胶有限公司 | Automatic rotary feeding device for plastic spool inserts |
| CN210308876U (en) * | 2019-06-21 | 2020-04-14 | 东莞市本润机器人科技股份有限公司 | Injection molding AOI check out test set |
| CN110977080A (en) * | 2019-12-27 | 2020-04-10 | 昆山华誉自动化科技有限公司 | Full-automatic annular PCB board and FPC soft board welding system |
| CN212433003U (en) * | 2020-08-28 | 2021-01-29 | 雷澳视觉科技(东莞)有限公司 | Automatic detection device for appearance defects of mobile phone iron frame |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112707175A (en) * | 2021-01-29 | 2021-04-27 | 常熟市龙腾滚动体制造有限公司 | End plate detection and stacking integrated discharging system |
| CN113848212A (en) * | 2021-10-25 | 2021-12-28 | 东莞市长智光视觉科技有限公司 | Inner cavity visual inspection machine and inner cavity detection method |
| CN114705685A (en) * | 2022-01-30 | 2022-07-05 | 中信云网有限公司 | AI visual detection method and system based on deep learning and readable storage medium |
| CN114705693A (en) * | 2022-01-30 | 2022-07-05 | 中信云网有限公司 | AI visual inspection device and system for shell structure defect detection |
| CN116973306A (en) * | 2023-04-24 | 2023-10-31 | 英业达(重庆)有限公司 | An appearance inspection device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111468433B (en) | Lens detection system and lens detection method | |
| CN110841932B (en) | A carton detection and sorting device | |
| CN212433003U (en) | Automatic detection device for appearance defects of mobile phone iron frame | |
| CN108303429A (en) | It is a kind of leaded light board defect automatically detection and sorting device | |
| CN211217581U (en) | Carton detects sorting device | |
| CN218691669U (en) | Automatic lighting detection device for secondary alignment pressure head automatic compensation crimping display screen | |
| CN115101433B (en) | Wafer surface defect detector | |
| CN110948840A (en) | A FPC circuit board automatic bending device | |
| CN212703136U (en) | Lens detecting system | |
| CN108557439B (en) | Plane object screening and discharging device | |
| CN110444491A (en) | A battery sheet IV, EL double-sided testing equipment | |
| CN113546853A (en) | Full-automatic visual detection sorting and discharging device | |
| CN111505011A (en) | Appearance testing equipment and testing method | |
| CN112268911A (en) | Mobile phone AOI detection equipment | |
| CN114799546A (en) | Full-automatic laser drilling method and equipment | |
| CN116214310A (en) | A ring integrated processing equipment | |
| CN116586316A (en) | A detection mounter | |
| CN106971957A (en) | A kind of surface defect screening installation of solar silicon wafers | |
| CN204866577U (en) | WiFi module calibration write number test integrated workstation | |
| CN116297522A (en) | A detection method combining appearance 2D and 3D and its application | |
| CN215542830U (en) | Flexible screen double-sided 3D detection equipment | |
| CN207946372U (en) | Glass defect automatic detection device | |
| CN108426611A (en) | Endoporus automatic detecting machine | |
| CN210120118U (en) | Battery piece IV, two-sided test equipment of EL | |
| CN117359957A (en) | Suction head and filter element assembly production line and working method thereof |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20201113 |
|
| RJ01 | Rejection of invention patent application after publication |