CN111667943A - A kind of photoelectric control composite shore power cable control core for ship and preparation method thereof - Google Patents
A kind of photoelectric control composite shore power cable control core for ship and preparation method thereof Download PDFInfo
- Publication number
- CN111667943A CN111667943A CN202010629596.7A CN202010629596A CN111667943A CN 111667943 A CN111667943 A CN 111667943A CN 202010629596 A CN202010629596 A CN 202010629596A CN 111667943 A CN111667943 A CN 111667943A
- Authority
- CN
- China
- Prior art keywords
- layer
- impact
- core
- wire core
- weaving
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images

Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B7/00—Insulated conductors or cables characterised by their form
- H01B7/0009—Details relating to the conductive cores
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B13/00—Apparatus or processes specially adapted for manufacturing conductors or cables
- H01B13/06—Insulating conductors or cables
- H01B13/14—Insulating conductors or cables by extrusion
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B13/00—Apparatus or processes specially adapted for manufacturing conductors or cables
- H01B13/22—Sheathing; Armouring; Screening; Applying other protective layers
- H01B13/24—Sheathing; Armouring; Screening; Applying other protective layers by extrusion
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B13/00—Apparatus or processes specially adapted for manufacturing conductors or cables
- H01B13/22—Sheathing; Armouring; Screening; Applying other protective layers
- H01B13/26—Sheathing; Armouring; Screening; Applying other protective layers by winding, braiding or longitudinal lapping
- H01B13/2606—Sheathing; Armouring; Screening; Applying other protective layers by winding, braiding or longitudinal lapping by braiding
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B7/00—Insulated conductors or cables characterised by their form
- H01B7/0045—Cable-harnesses
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B7/00—Insulated conductors or cables characterised by their form
- H01B7/17—Protection against damage caused by external factors, e.g. sheaths or armouring
- H01B7/18—Protection against damage caused by wear, mechanical force or pressure; Sheaths; Armouring
- H01B7/1875—Multi-layer sheaths
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01B—CABLES; CONDUCTORS; INSULATORS; SELECTION OF MATERIALS FOR THEIR CONDUCTIVE, INSULATING OR DIELECTRIC PROPERTIES
- H01B7/00—Insulated conductors or cables characterised by their form
- H01B7/17—Protection against damage caused by external factors, e.g. sheaths or armouring
- H01B7/18—Protection against damage caused by wear, mechanical force or pressure; Sheaths; Armouring
- H01B7/189—Radial force absorbing layers providing a cushioning effect
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Communication Cables (AREA)
Abstract
本发明提供一种舰船用光电控制复合岸电电缆控制线芯,包括内芯结构和外套结构,内芯结构包括多个导体、设置在每个导体内的抗拉层和设置在每个导体外的绝缘层;外套结构由内到外依次为第一抗冲击层、第一屏蔽层、第二抗冲击层、第二屏蔽层、第三抗冲击层、第三屏蔽层和包覆层;电缆内芯结构和外套结构之间设置填充层。本发明通过设计新型控制线芯导体,可有效避免控制线芯在频繁弯曲移动过程中的断芯,且断芯后不会对动力线芯产生破坏。
The invention provides a control wire core of an optoelectronic control composite shore power cable for ships, comprising an inner core structure and an outer shell structure, wherein the inner core structure includes a plurality of conductors, a tensile layer arranged in each conductor and a The outer insulating layer; the outer jacket structure from the inside to the outside is the first anti-impact layer, the first shielding layer, the second anti-impact layer, the second shielding layer, the third anti-impact layer, the third shielding layer and the cladding layer; A filler layer is arranged between the inner core structure and the outer jacket structure of the cable. By designing a new type of control wire core conductor, the present invention can effectively avoid the broken core of the control wire core during the frequent bending and moving process, and the power wire core will not be damaged after the broken core.
Description
技术领域technical field
本发明涉及一种配电电缆技术领域,尤其涉及一种舰船用光电控制复合岸电电缆控制线芯及其制备方法。The invention relates to the technical field of power distribution cables, in particular to a control wire core of a marine photoelectric control composite shore power cable and a preparation method thereof.
背景技术Background technique
大型舰船在到达港口时通常使用重油或柴油发电来满足舰船停泊时的用电需求,辅机在工作时燃烧大量的油料,排出大量的废气,同时24小时不间断地产生噪声污染,随着“低碳减排”的环保要求,采用舰船接入岸电使舰船在停靠码头期间不再依靠辅机发电,而是采用码头岸电系统开始对停靠舰船供电来代替辅机发电,舰船用光电控制复合岸电电缆在使用过程中反复频繁地收放、卷绕、拖拽、冲击场合时的电源连接,电缆在反复频繁地收放、卷绕、拖拽、冲击使用时,线芯易打扭、断芯,并且线芯打扭、断芯处局部温度过高造成主线芯的击穿。Large ships usually use heavy oil or diesel to generate electricity when they arrive at the port to meet the electricity demand of ships when they are berthing. Auxiliary engines burn a lot of oil and discharge a lot of waste gas when working, and at the same time, they generate noise pollution 24 hours a day. In line with the environmental protection requirements of "low carbon emission reduction", the use of ship access to shore power enables ships to no longer rely on auxiliary engines to generate electricity during docking, but to use the dock shore power system to start supplying power to docked ships instead of auxiliary engines for power generation. , The power connection of the ship's photoelectric control composite shore power cable is repeatedly and frequently retracted, wound, dragged, and impacted during use. , the wire core is easily twisted and broken, and the local temperature at the twisted and broken core of the wire core is too high, causing the breakdown of the main wire core.
发明内容SUMMARY OF THE INVENTION
本发明的目的是在于克服、补充现有技术中存在的不足,提供一种舰船用光电控制复合岸电电缆控制线芯及其制备方法,使线芯在反复频繁地收放、卷绕、拖拽、冲击使用时,控制线芯不打扭、不断芯,且出现打扭、断芯时不会引起主线芯的击穿。本发明的技术方案为:The purpose of the present invention is to overcome and supplement the deficiencies in the prior art, and to provide a control wire core of a photoelectric control composite shore power cable for ships and a preparation method thereof, so that the wire core can be repeatedly and frequently retracted, wound, When used by dragging and impacting, the control wire core will not be twisted or broken, and the main wire core will not be broken down when twisted or broken. The technical scheme of the present invention is:
一种舰船用光电控制复合岸电电缆控制线芯,其中:包括内芯结构和外套结构,所述内芯结构包括多个导体、设置在每个所述导体内的抗拉层和设置在每个所述导体外的绝缘层;A control wire core of a marine photoelectric control composite shore power cable, which includes an inner core structure and an outer shell structure, the inner core structure includes a plurality of conductors, a tensile layer arranged in each of the conductors, and a an insulating layer outside each of said conductors;
所述外套结构由内到外依次为第一抗冲击层、第一屏蔽层、第二抗冲击层、第二屏蔽层、第三抗冲击层、第三屏蔽层和包覆层;The outer jacket structure is, from inside to outside, a first anti-impact layer, a first shielding layer, a second anti-impact layer, a second shielding layer, a third anti-impact layer, a third shielding layer and a cladding layer in sequence;
所述电缆内芯结构和外套结构之间设置填充层。A filling layer is arranged between the inner core structure and the outer jacket structure of the cable.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯,其中:所述多个导体在内芯结构横截面围成圆形。Preferably, in the control wire core of the ship's photoelectric control composite shore power cable, wherein: the plurality of conductors enclose a circle in the cross section of the inner core structure.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯,其中:所述抗拉层的材质为对位芳纶长丝,所述绝缘层的材质为三元乙丙橡胶。Preferably, in the control core of the marine photoelectric control composite shore power cable, the material of the tensile layer is para-aramid filament, and the material of the insulating layer is EPDM.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯,其中:所述第一抗冲击层、第二抗冲击层、第三抗冲击层的材质为芳纶短切纤维,所述第一屏蔽层、第二屏蔽层、第三屏蔽层的材质为石墨烯,所述包覆层的材质为氯丁橡胶。Preferably, in the control core of the ship's photoelectric control composite shore power cable, wherein: the first impact-resistant layer, the second impact-resistant layer, and the third impact-resistant layer are made of aramid chopped fibers, The first shielding layer, the second shielding layer, and the third shielding layer are made of graphene, and the coating layer is made of neoprene.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯,其中:每个所述导体均包括第一线芯和设置在第一线芯外的第二线芯,所述第一线芯由16束第一绞线编织而成,每束第一绞线包括5根镀锡铜丝;所述第二线芯由16束第二绞线编织而成,每束第二绞线包括6根镀锡铜丝;每根所述镀锡铜丝的横截面的直径设置为0.1-0.2mm。Preferably, in the control wire core of the marine photoelectric control composite shore power cable, wherein: each of the conductors includes a first wire core and a second wire core disposed outside the first wire core, the first wire core The core is woven from 16 bundles of first stranded wires, each bundle of which includes 5 tinned copper wires; the second core is woven from 16 bundles of second stranded wires, and each bundle of second stranded wires includes 6 tinned copper wires; the diameter of the cross section of each of the tinned copper wires is set to 0.1-0.2 mm.
一种舰船用光电控制复合岸电电缆控制线芯的制备方法,其中:包括以下步骤:A method for preparing a control core of a photoelectric control composite shore power cable for ships, comprising the following steps:
1)将抗拉层外通过编织机编织导体,并在导体外挤包绝缘层,然后将将包覆绝缘层的多个导体加入填充剂成缆形成内芯结构;1) Braid the conductor through the braiding machine outside the tensile layer, and extrude the insulating layer outside the conductor, and then add the multiple conductors covered with the insulating layer to the filler to form a cable to form an inner core structure;
2)将内芯结构外通过编织机进行编织第一抗冲击层,将编织好的第一抗冲击层以0.5-1.5m/min的线速度通过涂覆装置,涂覆第一屏蔽层;2) Weaving the first impact-resistant layer outside the inner core structure through a braiding machine, and passing the braided first impact-resistant layer through a coating device at a linear speed of 0.5-1.5 m/min to coat the first shielding layer;
3)将第一屏蔽层外通过编织机进行编织第二抗冲击层,将编织好的第二抗冲击层以0.5-1.5m/min的线速度通过涂覆装置,涂覆第二屏蔽层;3) Weaving the second impact-resistant layer outside the first shielding layer through a braiding machine, and passing the braided second impact-resistant layer through the coating device at a linear speed of 0.5-1.5 m/min to coat the second shielding layer;
4)将第二屏蔽层外通过编织机进行编织第三抗冲击层,将编织好的第三抗冲击层以0.5-1.5m/min的线速度通过涂覆装置,涂覆第三屏蔽层;4) Weaving the third impact-resistant layer outside the second shielding layer through a braiding machine, and passing the braided third impact-resistant layer through the coating device at a linear speed of 0.5-1.5 m/min to coat the third shielding layer;
5)将第三屏蔽层外挤包一层包覆层,得到舰船用光电控制复合岸电电缆控制线芯。5) The third shielding layer is extruded and wrapped with a cladding layer to obtain the control core of the ship's photoelectric control composite shore power cable.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯的制备方法,其中:所述步骤1)导体包括第一线芯和第二线芯,控制第一线芯编织密度为90-92%,编织角为45-55°,然后在第一线芯外编织第二线芯,控制第二线芯编织密度在80-82%,编织角为55-60°。Preferably, in the method for preparing the control wire core of the photoelectric control composite shore power cable for ships, wherein: the step 1) the conductor includes a first wire core and a second wire core, and the weaving density of the first wire core is controlled to be 90 -92%, the braiding angle is 45-55°, and then the second core is braided outside the first core, the braiding density of the second core is controlled at 80-82%, and the braiding angle is 55-60°.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯的制备方法,其中:所述抗拉层的材质为对位芳纶长丝,所述绝缘层的材质为三元乙丙橡胶。Preferably, in the method for preparing the control wire core of the photoelectric control composite shore power cable for ships, wherein: the material of the tensile layer is para-aramid filament, and the material of the insulating layer is ternary ethylene Propylene rubber.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯的制备方法,其中:所述第一抗冲击层、第二抗冲击层、第三抗冲击层的材质为芳纶短切纤维;所述第一屏蔽层、第二屏蔽层、第三屏蔽层的材质为石墨烯,每层厚度为0.1~0.25mm;所述包覆层的材质为氯丁橡胶。Preferably, in the preparation method of the control core of the ship photoelectric control composite shore power cable, wherein: the first impact-resistant layer, the second impact-resistant layer, and the third impact-resistant layer are made of short aramid fibers Cut fibers; the material of the first shielding layer, the second shielding layer and the third shielding layer is graphene, and the thickness of each layer is 0.1-0.25 mm; the material of the coating layer is neoprene.
优选的是,所述的舰船用光电控制复合岸电电缆控制线芯的制备方法,其中:所述第一抗冲击层编织密度控制在80-82%,编织角为55-60°;第二抗冲击层编织密度控制在88-90%,编织角为55-60°;第三抗冲击层编织密度控制在98-100%,编织角为35-40°。Preferably, in the method for preparing the control core of the composite shore power cable with photoelectric control for ships, the braiding density of the first impact-resistant layer is controlled at 80-82%, and the braiding angle is 55-60°; The weave density of the second impact-resistant layer is controlled at 88-90%, and the weave angle is 55-60°; the weave density of the third impact-resistant layer is controlled at 98-100%, and the weave angle is 35-40°.
本发明的优点:Advantages of the present invention:
(1)本发明通过设计新型控制线芯导体,可有效避免控制线芯在频繁弯曲移动过程中的断芯,且断芯后不会对动力线芯产生破坏。(1) The present invention can effectively avoid core breakage of the control wire core during frequent bending and movement by designing a new type of control wire core conductor, and the power wire core will not be damaged after the broken core.
(2)本发明的舰船用光电控制复合岸电电缆控制线芯,包括内芯结构和外套结构,内芯结构包括多个导体,每个导体内均设置抗拉层,导体经编织后,耐扭、抗拉性能明显提高;外套结构由内到外依次为第一抗冲击层、第一屏蔽层、第二抗冲击层、第二屏蔽层、第三抗冲击层、第三屏蔽层和包覆层,三层抗冲击层材质均为对位芳纶短切纤维,可有效抵御外部冲击,当控制线芯发生断芯后,三层对位芳纶短切纤维可有效将控制线芯导体包覆其中,而不会有断丝扎伤动力线芯,造成动力线芯的击穿,通过设置三层屏蔽层可有效替代镀锡铜丝编织屏蔽,使得对位芳纶短切纤维编织既可以起到抗拉、抗冲击,且屏蔽效果更佳。(2) The control core of the photoelectric control composite shore power cable for ships of the present invention includes an inner core structure and an outer shell structure. The inner core structure includes a plurality of conductors, and each conductor is provided with a tensile layer. After the conductors are woven, The torsion resistance and tensile performance are significantly improved; the outer jacket structure is sequentially composed of the first impact-resistant layer, the first shielding layer, the second impact-resistant layer, the second shielding layer, the third impact-resistant layer, the third shielding layer and the The covering layer and the three-layer impact-resistant layer are made of para-aramid chopped fibers, which can effectively resist external impact. The conductor is wrapped in it, and there will be no broken wire to hurt the power core, which will cause the breakdown of the power core. By setting three layers of shielding layers, it can effectively replace the braided shield of tinned copper wire, so that the braided para-aramid chopped fiber can be braided. It can not only play tensile and impact resistance, but also has better shielding effect.
附图说明Description of drawings
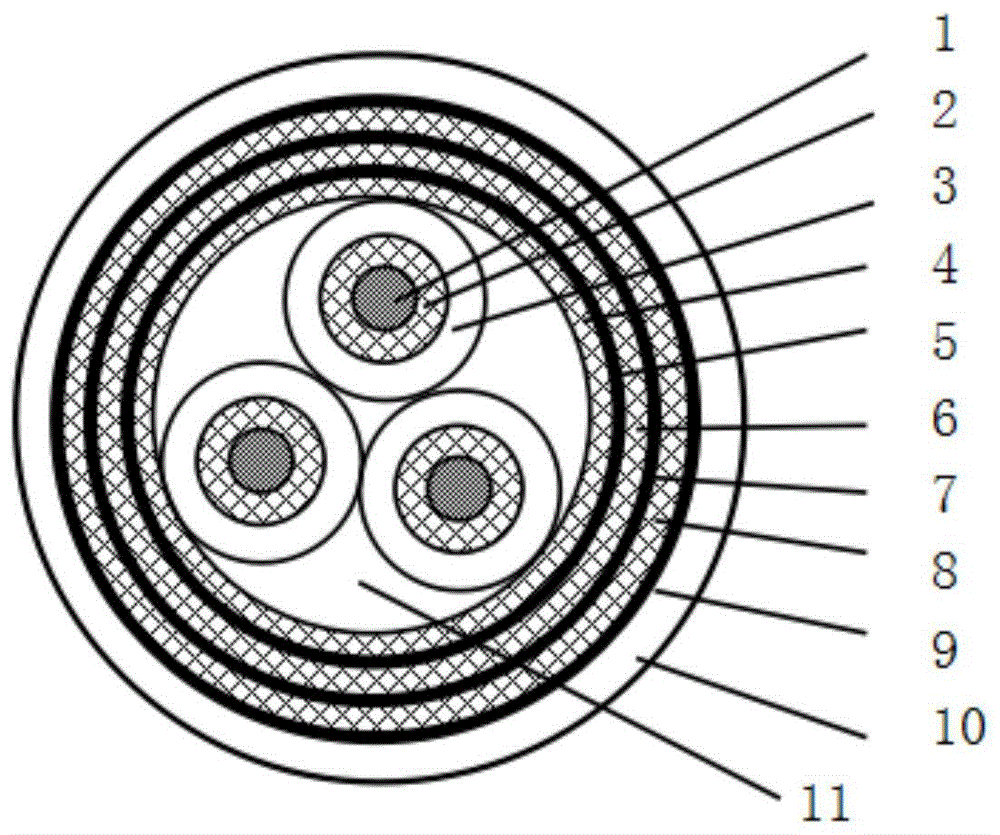
图1为本发明舰船用光电控制复合岸电电缆控制线芯的结构示意图。FIG. 1 is a schematic structural diagram of the control core of the marine photoelectric control composite shore power cable according to the present invention.
具体实施方式Detailed ways
下面结合具体实施例对本发明作进一步说明。The present invention will be further described below in conjunction with specific embodiments.
实施例1:Example 1:
如图1所示,一种舰船用光电控制复合岸电电缆控制线芯,其中:包括内芯结构和外套结构,所述内芯结构包括多个导体2、设置在每个所述导体2内的抗拉层1和设置在每个所述导体外的绝缘层3;As shown in FIG. 1 , a control core of a marine photoelectric control composite shore power cable includes an inner core structure and an outer shell structure, and the inner core structure includes a plurality of
所述外套结构由内到外依次为第一抗冲击层4、第一屏蔽层5、第二抗冲击层6、第二屏蔽层7、第三抗冲击层8、第三屏蔽层9和包覆层10;The outer jacket structure is, from inside to outside, a first impact-
所述电缆内芯结构和外套结构之间设置填充层11。A
所述多个导体2在内芯结构横截面围成圆形;所述抗拉层的材质为对位芳纶长丝,所述绝缘层的材质为三元乙丙橡胶;所述第一抗冲击层、第二抗冲击层、第三抗冲击层的材质为芳纶短切纤维,所述第一屏蔽层、第二屏蔽层、第三屏蔽层的材质为石墨烯,所述包覆层的材质为氯丁橡胶;每个所述导体2均包括第一线芯和设置在第一线芯外的第二线芯,所述第一线芯由16束第一绞线编织而成,每束第一绞线包括5根镀锡铜丝;所述第二线芯由16束第二绞线编织而成,每束第二绞线包括6根镀锡铜丝;每根所述镀锡铜丝的横截面的直径设置为0.1-0.2mm。The plurality of
实施例2:Example 2:
一种舰船用光电控制复合岸电电缆控制线芯的制备方法,其中:包括以下步骤:A method for preparing a control core of a photoelectric control composite shore power cable for ships, comprising the following steps:
1)将5股2000dtex的对位芳纶长丝进行填充作为抗拉层,抗拉层外通过编织机编织导体,并在导体外挤包绝缘层,然后将三个导体加入填充剂成缆形成内芯结构,成缆节距比控制在6倍以内;1) Fill 5 strands of 2000dtex para-aramid filaments as a tensile layer, braid the conductors through a braiding machine outside the tensile layer, and extrude an insulating layer outside the conductors, and then add fillers to the three conductors to form a cable Inner core structure, the cabling pitch ratio is controlled within 6 times;
2)将内芯结构外通过编织机进行编织第一抗冲击层,将编织好的第一抗冲击层以0.5-1.5m/min的线速度通过石墨烯涂覆装置,涂覆0.1-0.25mm的第一屏蔽层;2) Weaving the first impact-resistant layer through a braiding machine outside the inner core structure, passing the woven first impact-resistant layer through a graphene coating device at a linear speed of 0.5-1.5m/min, and coating 0.1-0.25mm the first shielding layer;
3)将第一屏蔽层外通过编织机进行编织第二抗冲击层,将编织好的第二抗冲击层以0.5-1.5m/min的线速度通过石墨烯涂覆装置,涂覆0.1-0.25mm第二屏蔽层;3) Weaving the second impact-resistant layer through the braiding machine outside the first shielding layer, passing the braided second impact-resistant layer through the graphene coating device at a linear speed of 0.5-1.5 m/min, and coating 0.1-0.25 mm second shielding layer;
4)将第二屏蔽层外通过编织机进行编织第三抗冲击层,将编织好的第三抗冲击层以0.5-1.5m/min的线速度通过石墨烯涂覆装置,涂覆0.1-0.25mm第三屏蔽层;4) Weaving the third impact-resistant layer through the braiding machine outside the second shielding layer, passing the braided third impact-resistant layer through the graphene coating device at a linear speed of 0.5-1.5 m/min, and coating 0.1-0.25 mm third shielding layer;
5)将第三屏蔽层外挤包一层包覆层,得到舰船用光电控制复合岸电电缆控制线芯。5) The third shielding layer is extruded and wrapped with a cladding layer to obtain the control core of the ship's photoelectric control composite shore power cable.
所述步骤1)导体包括第一线芯和第二线芯,第一线芯采用16锭编织机进行编织,每锭5根0.15mm的镀锡铜丝,控制第一线芯编织密度为90-92%,编织角为45-55°,然后在第一线芯外编织第二线芯,第二线芯同样采用16锭编织机进行编织,每锭6根0.15mm的镀锡铜丝,控制第二线芯编织密度在80-82%,编织角为55-60°。Step 1) The conductor includes a first wire core and a second wire core, the first wire core is woven with a 16-spindle braiding machine, and each ingot is 5 tinned copper wires of 0.15 mm, and the weaving density of the first wire core is controlled to be 90- 92%, the braiding angle is 45-55°, and then the second wire core is braided outside the first wire core. The second wire core is also braided by a 16-spindle braiding machine, with 6 tinned copper wires of 0.15mm per spindle to control the second wire. The core weave density is 80-82%, and the weave angle is 55-60°.
所述抗拉层的材质为对位芳纶长丝,所述绝缘层的材质为三元乙丙橡胶。The material of the tensile layer is para-aramid filament, and the material of the insulating layer is EPDM rubber.
对位芳纶长丝的性能指标如表1:The performance index of para-aramid filament is shown in Table 1:
表1Table 1

控制线芯导体经编织后,耐扭、抗拉性能明显提高,控制线芯导体性能对比如表2:After the control core conductor is braided, the torsion resistance and tensile strength are significantly improved. The performance comparison of the control core conductor is shown in Table 2:
表2Table 2

经样机反复试验,最终确定采用对位芳纶长丝进行填充,外层两次编织的控制线芯导体,抗拉,耐扭性能最优越,且单位重量较轻。After repeated tests of the prototype, it was finally determined that the para-aramid filament was used for filling, and the outer layer was braided twice as a control core conductor, which had the best tensile and torsional properties, and had a lighter unit weight.
所述第一抗冲击层、第二抗冲击层、第三抗冲击层的材质为芳纶短切纤维;所述第一屏蔽层、第二屏蔽层、第三屏蔽层的材质为石墨烯,每层厚度为0.1~0.25mm;所述包覆层的材质为氯丁橡胶。The first impact-resistant layer, the second impact-resistant layer, and the third impact-resistant layer are made of aramid chopped fibers; the first shielding layer, the second shielding layer, and the third shielding layer are made of graphene. The thickness of each layer is 0.1-0.25 mm; the material of the coating layer is neoprene.
控制线芯成缆后编织三层对位芳纶短切纤维,第一层采用16锭编织机进行编织,每锭1股1000dtex的对位芳纶短切纤维,编织密度控制在80-82%,编织角55-60°,第二层采用16锭编织机进行编织,每锭1股1000dtex的对位芳纶短切纤维,编织密度控制在88-90%,编织角55-60°,第三层采用16锭编织机进行编织,每锭2股1000dtex的对位芳纶短切纤维,编织密度控制在98-100%,编织角35-40°,对位芳纶短切纤维性能如表3:After the control core is cabled, three layers of para-aramid chopped fibers are braided. The first layer is braided by a 16-spindle braiding machine. Each spindle is 1 strand of 1000dtex para-aramid chopped fibers, and the weaving density is controlled at 80-82%. , the braiding angle is 55-60°, the second layer is braided by a 16-spindle braiding machine, each spindle is 1 strand of 1000dtex para-aramid chopped fiber, the braiding density is controlled at 88-90%, the braiding angle is 55-60°, the first The three layers are braided by a 16-spindle braiding machine. Each spindle has 2 strands of 1000dtex para-aramid chopped fibers. The weaving density is controlled at 98-100%, and the braiding angle is 35-40°. The properties of the para-aramid chopped fibers are shown in the table below. 3:
表3:table 3:

采用强度更高的对位芳纶短切纤维可有效提高控制线芯成缆后的整体拉断力,且对位芳纶短切纤维的卷曲回复率较高,当控制线芯受到外部冲击力时,三层对位芳纶短切纤维可有效抵御外部冲击,当控制线芯发生断芯后,三层对位芳纶短切纤维可有效将控制线芯导体包覆其中,而不会有断丝扎伤动力线芯,造成动力线芯的击穿。The use of para-aramid chopped strands with higher strength can effectively improve the overall breaking force of the control core after cabling, and the crimp recovery rate of para-aramid chopped strands is high. When the control core is subjected to an external impact force When the control core is broken, the three layers of para-aramid chopped fibers can effectively cover the conductor of the control core without any The broken wire hurts the power core, resulting in the breakdown of the power core.
对位芳纶短切纤维每层编织后涂覆一层石墨烯,将编织好的控制线芯以0.5-1.5m/min的线速度通过转入1000-2000转/min的石墨烯涂覆装置,控制石墨烯的厚度控制在0.1-0.25mm之间,对位芳纶短切纤维涂覆石墨烯可有效替代镀锡铜丝编织屏蔽,对位芳纶短切纤维编织既可以起到抗拉、抗冲击,且屏蔽效果更佳,内芯结构外设置第一抗冲击层、第一屏蔽层、第二抗冲击层、第二屏蔽层、第三抗冲击层、第三屏蔽层,其测试性能如表4:Each layer of para-aramid chopped fibers is woven and coated with a layer of graphene, and the woven control core is transferred to a graphene coating device of 1000-2000 rpm at a linear speed of 0.5-1.5m/min. , control the thickness of graphene to be controlled between 0.1-0.25mm, the para-aramid chopped fiber coating graphene can effectively replace the tinned copper wire braided shield, the para-aramid chopped fiber braiding can not only play a tensile strength , impact resistance, and the shielding effect is better, the first impact resistance layer, the first shielding layer, the second impact resistance layer, the second shielding layer, the third impact resistance layer and the third shielding layer are arranged outside the inner core structure. The performance is shown in Table 4:
表4:Table 4:

第三屏蔽层外挤包一层性能优异的氯丁橡胶对石墨烯材料进行包覆,包覆后频繁的弯曲,移动,石墨烯材料不脱落,屏蔽效果可长期优异,线芯的整体抗拉强度、抗冲击性能如表5:The third shielding layer is extruded with a layer of neoprene rubber with excellent performance to coat the graphene material. After coating, it is frequently bent and moved, and the graphene material does not fall off. The shielding effect can be excellent for a long time. The overall tensile strength of the wire core The strength and impact resistance are shown in Table 5:
表5:table 5:
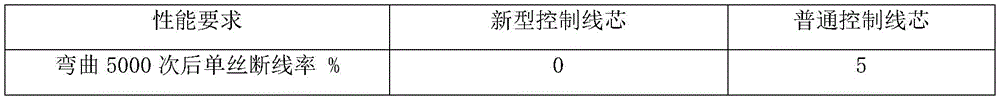

从表5可以看出,线芯的抗断芯性能、抗拉强度较普通控制线芯均有明显的提高,说明本发明舰船用光电控制复合岸电电缆控制线芯,可有效避免控制线芯在频繁弯曲移动过程中的断芯,且断芯后不会对动力线芯产生破坏。It can be seen from Table 5 that the core breaking resistance and tensile strength of the core are significantly improved compared with the ordinary control core, indicating that the control core of the ship photoelectric control composite shore power cable can effectively avoid the control wire The core is broken during frequent bending and moving, and the power wire core will not be damaged after the core is broken.
最后所应说明的是,以上具体实施方式仅用以说明本发明的技术方案而非限制,尽管参照实例对本发明进行了详细说明,本领域的普通技术人员应当理解,可以对本发明的技术方案进行修改或者等同替换,而不脱离本发明技术方案的精神和范围,其均应涵盖在本发明的权利要求范围当中。Finally, it should be noted that the above specific embodiments are only used to illustrate the technical solutions of the present invention and not to limit them. Although the present invention has been described in detail with reference to examples, those of ordinary skill in the art should understand that the technical solutions of the present invention can be Modifications or equivalent substitutions without departing from the spirit and scope of the technical solutions of the present invention should be included in the scope of the claims of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010629596.7A CN111667943A (en) | 2020-07-03 | 2020-07-03 | A kind of photoelectric control composite shore power cable control core for ship and preparation method thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010629596.7A CN111667943A (en) | 2020-07-03 | 2020-07-03 | A kind of photoelectric control composite shore power cable control core for ship and preparation method thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111667943A true CN111667943A (en) | 2020-09-15 |
Family
ID=72390907
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010629596.7A Pending CN111667943A (en) | 2020-07-03 | 2020-07-03 | A kind of photoelectric control composite shore power cable control core for ship and preparation method thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111667943A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119763908A (en) * | 2024-12-31 | 2025-04-04 | 广州市力可欣电子有限公司 | Layered knitting control wire and manufacturing method thereof |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2018027534A1 (en) * | 2016-08-09 | 2018-02-15 | 广州市雷曼兄弟电子科技有限公司 | Data line |
| CN207676673U (en) * | 2017-12-07 | 2018-07-31 | 江苏新远程电缆有限公司 | A kind of naval vessel, which is used up, replies conjunction immediate frequency cable by cable |
| CN208173265U (en) * | 2018-03-20 | 2018-11-30 | 南通智博电子线缆有限公司 | Flexible Drag shielding control cable |
| CN109036668A (en) * | 2018-08-04 | 2018-12-18 | 安徽华能电缆集团有限公司 | A kind of tension power cable |
| KR20180135542A (en) * | 2017-06-13 | 2018-12-21 | 엘에스전선 주식회사 | Cable for warship |
| CN212322653U (en) * | 2020-07-03 | 2021-01-08 | 江苏中煤电缆有限公司 | Photoelectric control composite shore power cable control wire core for ships |
-
2020
- 2020-07-03 CN CN202010629596.7A patent/CN111667943A/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2018027534A1 (en) * | 2016-08-09 | 2018-02-15 | 广州市雷曼兄弟电子科技有限公司 | Data line |
| KR20180135542A (en) * | 2017-06-13 | 2018-12-21 | 엘에스전선 주식회사 | Cable for warship |
| CN207676673U (en) * | 2017-12-07 | 2018-07-31 | 江苏新远程电缆有限公司 | A kind of naval vessel, which is used up, replies conjunction immediate frequency cable by cable |
| CN208173265U (en) * | 2018-03-20 | 2018-11-30 | 南通智博电子线缆有限公司 | Flexible Drag shielding control cable |
| CN109036668A (en) * | 2018-08-04 | 2018-12-18 | 安徽华能电缆集团有限公司 | A kind of tension power cable |
| CN212322653U (en) * | 2020-07-03 | 2021-01-08 | 江苏中煤电缆有限公司 | Photoelectric control composite shore power cable control wire core for ships |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119763908A (en) * | 2024-12-31 | 2025-04-04 | 广州市力可欣电子有限公司 | Layered knitting control wire and manufacturing method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN205881496U (en) | Full carbon light cable | |
| CN205692585U (en) | Flexible new-energy automobile charging pile cable | |
| CN201667241U (en) | New Armored Submarine Cable | |
| WO2022021623A1 (en) | High and low temperature resistant anti-interference integrated flexible cable for unmanned aerial vehicle | |
| CN213716584U (en) | Light high-current-carrying tensile anti-torsion liquid-cooled charging cable for direct-current charging pile | |
| CN202102770U (en) | Environment-friendly flexible cable used for torsion-resisting roll canister machine | |
| CN110459344A (en) | Reel control cable and manufacturing method thereof | |
| CN110232994A (en) | The super soft high reliability welding robot feed cable of one kind and preparation method | |
| CN212847745U (en) | 24 drag low frequency signal transmission cable for ocean | |
| CN201717025U (en) | Towing chain cable | |
| CN114068061A (en) | Flexible cable for 10MW offshore wind generating set and preparation method thereof | |
| CN212322653U (en) | Photoelectric control composite shore power cable control wire core for ships | |
| CN208061689U (en) | A kind of wisdom energy port machine low pressure spool cable | |
| CN218497810U (en) | Photoelectric composite flexible high-voltage reel cable for port power supply | |
| CN115631884B (en) | Tensile torsion-resistant medium-voltage cable for wind driven generator and preparation method thereof | |
| CN201584202U (en) | Power supply flexible cable for crossing over boat body of open dredge boat | |
| CN116741457A (en) | Tensile torsion-resistant 66kV high-voltage cable for offshore wind power generation and preparation method thereof | |
| CN205692590U (en) | Tensile type wind generator system flexible cable | |
| CN214043117U (en) | 35kV and below flexible cable that warp resistance is used in wind power generation | |
| CN214476567U (en) | Single-core tensile flexible cable | |
| CN209880209U (en) | USB electric wire shielding braided structure for increasing tensile property | |
| CN209543975U (en) | Composite control cable for mine conveying machinery | |
| CN212322723U (en) | Photoelectric composite longitudinal watertight cable | |
| CN210006482U (en) | control cable for bending-resistant EMC system | |
| CN209822334U (en) | A tensile and flame-retardant control cable |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200915 |