CN111644834B - Detachable truss screw machine - Google Patents
Detachable truss screw machine Download PDFInfo
- Publication number
- CN111644834B CN111644834B CN202010506545.5A CN202010506545A CN111644834B CN 111644834 B CN111644834 B CN 111644834B CN 202010506545 A CN202010506545 A CN 202010506545A CN 111644834 B CN111644834 B CN 111644834B
- Authority
- CN
- China
- Prior art keywords
- stepping
- screw
- track
- rail
- pressing plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003825 pressing Methods 0.000 claims abstract description 57
- 238000004080 punching Methods 0.000 claims abstract description 28
- 230000007246 mechanism Effects 0.000 claims abstract description 24
- 239000000463 material Substances 0.000 claims abstract description 13
- 238000007599 discharging Methods 0.000 claims description 13
- 230000001939 inductive effect Effects 0.000 claims description 5
- 230000000149 penetrating effect Effects 0.000 claims description 3
- 238000000034 method Methods 0.000 abstract description 6
- 230000008569 process Effects 0.000 abstract description 6
- 230000001429 stepping effect Effects 0.000 description 35
- 238000010586 diagram Methods 0.000 description 5
- 230000005540 biological transmission Effects 0.000 description 4
- 238000003754 machining Methods 0.000 description 4
- 238000006073 displacement reaction Methods 0.000 description 3
- 229910000831 Steel Inorganic materials 0.000 description 2
- 239000004568 cement Substances 0.000 description 2
- 230000002265 prevention Effects 0.000 description 2
- 239000010959 steel Substances 0.000 description 2
- 238000007792 addition Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P19/00—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes
- B23P19/04—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes for assembling or disassembling parts
- B23P19/06—Screw or nut setting or loosening machines
- B23P19/069—Multi-spindle machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23B—TURNING; BORING
- B23B39/00—General-purpose boring or drilling machines or devices; Sets of boring and/or drilling machines
- B23B39/16—Drilling machines with a plurality of working-spindles; Drilling automatons
- B23B39/161—Drilling machines with a plurality of working-spindles; Drilling automatons with parallel work spindles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23B—TURNING; BORING
- B23B41/00—Boring or drilling machines or devices specially adapted for particular work; Accessories specially adapted therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P19/00—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes
- B23P19/001—Article feeders for assembling machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P19/00—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes
- B23P19/001—Article feeders for assembling machines
- B23P19/004—Feeding the articles from hoppers to machines or dispensers
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Press Drives And Press Lines (AREA)
- Machine Tool Units (AREA)
Abstract
The invention relates to an assembly machine, in particular to a detachable truss screw machine which comprises a base, a stepping mechanism, a feeding mechanism and a processing mechanism, wherein the stepping mechanism comprises a stepping track and a stepping pressing plate device, the processing mechanism comprises a fixing frame, a punching device, a screw feeding device and a screw feeding machine, the feeding mechanism comprises a main track and auxiliary tracks parallel to the main track, vibration discs are arranged at two ends of the main track, a material placing groove is connected onto each vibration disc, a transfer device is arranged beside the material placing groove, a plurality of moving jigs matched with the transfer device and capable of moving along the main track are arranged on the main track, a pushing cylinder is arranged on each auxiliary track, a clamp is connected to one side, facing the main track, of each pushing cylinder, a control screen is arranged on the fixing frame, and the control screens are respectively connected with the stepping pressing plate device, the punching device, the screw feeding device, the transfer device and the pushing cylinder. The invention saves the manual process of feeding, realizes full automation of the processing process, and has high processing efficiency and high precision of the processed finished product.
Description
Technical Field
The invention relates to a screw assembling machine, in particular to a detachable truss screw machine.
Background
When the truss floor support plate is produced, the truss needs to be welded firstly, then the steel bar truss is welded on the bottom plate, and finally cement is poured for forming. The existing production method of the truss floor support plate comprises the steps of fixing a truss fixing seat on a bottom plate through screws, welding a steel bar truss on the truss fixing seat, and taking down the bottom plate after pouring cement. The bottom plate is bulky, and the kind is also different mostly, therefore traditional screw assembly machine can't be suitable for, so often need artifical the completion with the process of truss fixing base fixed to the bottom plate, wastes time and energy.
The Chinese patent with publication No. CN 208644595UU discloses an automatic screw assembling machine, which comprises a conveying device, a screw loading device arranged on the conveying device and a workbench matched with the conveying device, wherein the conveying device comprises a frame, a conveying guide rail is arranged on the frame, the screw loading device is fixedly arranged on the frame, one side of the screw loading device is provided with an extension bracket, a drilling drive and a drill bit, the screw loading device comprises a supporting base, fix the support frame on the support base, fix drive arrangement on the support frame and the processing agency who is connected with drive arrangement, processing framework includes a plurality of telescopic cylinder of fixing in the support frame front portion and installs the screwdriver in telescopic cylinder below, and the workstation includes that support plate and a plurality of positioning seats of setting perpendicularly at the support plate upper surface, and it has integrated into one piece to put the thing groove to open on the positioning seat, and the support plate lower fixed surface has the card foot that matches with transfer guide. Compared with the prior processing technology, the automatic screw assembling machine has the advantages of high processing speed and labor saving. However, the automatic screw assembling machine has many disadvantages, for example, the feeding still needs manual operation, the efficiency is actually not high, and the labor cost is not low; stability during processing can not be guaranteed, and the processing position is inaccurate because of vibrations or displacement easily when punching or go up the screw for the truss bottom plate.
Disclosure of Invention
The invention aims to overcome the defects in the prior art, and provides a detachable truss screw machine.
The technical scheme adopted by the invention for solving the technical problem is as follows:
the utility model provides a removable truss screw machine, includes base and step mechanism, feeding mechanism and the processing agency of setting on the base, its characterized in that: the stepping mechanism comprises a stepping track fixed with the base and stepping pressure plate devices arranged on two sides of the stepping track, and the stepping track is provided with a feeding end and a discharging end; the processing mechanism comprises a fixed frame which is fixed with the base and positioned above the stepping track, a punching device which is arranged on one side of the fixed frame towards the feeding end, a screw feeding device which is arranged on one side of the fixed frame towards the discharging end and corresponds to the punching device, and a screw feeding machine which is arranged beside the fixed frame and is connected with the screw feeding device; the feeding structure comprises a main rail fixed on the base and penetrating through the lower part of the stepping rail and an auxiliary rail fixed on the base and parallel to the main rail, vibration discs are symmetrically arranged at two ends of the main rail, a material placing groove opposite to the main rail is connected to the vibration discs, a corresponding transfer device is arranged beside the material placing groove, a plurality of moving jigs matched with the transfer device and capable of moving along the main rail are arranged on the main rail, a pushing cylinder capable of moving along the auxiliary rail is arranged on the auxiliary rail, and a fixture matched with the moving jigs is connected to one side, facing the main rail, of the pushing cylinder; the control screen towards the feeding end is arranged on the fixing frame and is respectively connected with the stepping pressing plate device, the punching device, the screw feeding device, the transferring device and the pushing cylinder.
Furthermore, the stepping pressing plate device comprises a pressing plate rail fixed with the base, a movable pressing seat arranged on the pressing plate rail and capable of moving along the pressing plate rail, a plurality of pressing plate cylinders arranged on the movable pressing seat and facing the stepping rail, and stepping pressing plates fixed on the pressing plate cylinders.
Furthermore, a limiting seat is further arranged between the stepping track and the pressing plate track, and a plurality of limiting idler wheels are fixed on the limiting seat.
Furthermore, the mount is provided with to feed end one side and prevents moving back the device, prevents moving back the device including preventing moving back the cylinder and connecting at the dog that prevents moving back the cylinder lower part.
Furthermore, the mount is provided with the feeding presser device that is located between anti-moving back device and the perforating device to feed end one side, and the feeding presser device is including the cylinder and the clamp plate that punches of connection in the cylinder lower part of punching.
Furthermore, the fixing frame is provided with a discharging pressure plate device towards one side of the discharging end, and the discharging pressure plate device comprises a screw cylinder and a screw pressure plate, wherein the screw cylinder is positioned beside the upper screw device, and the screw pressure plate is connected to the lower portion of the screw cylinder.
Furthermore, an inductive switch connected with the control screen is arranged on the stepping track.
Further, transfer device is including fixing on the base and being on a parallel with the transfer track of primary rail, setting on transferring the track and with the lifting mechanical hand that removes the tool matching, lifting mechanical hand bottom is provided with the card rod.
Furthermore, a positioning seat matched with the fixture is arranged at the lower part of the transfer track.
Furthermore, a movable structure which is movably connected with the main rail and is positioned right below the upper screw device is arranged in the middle of the main rail, and a jig lifting device which is fixed with the movable structure is arranged right below the movable structure.
Compared with the prior art, the invention has the following advantages and effects: the structure is scientific, the manual loading process is saved, the full automation of the machining process is realized, and the machining efficiency is high; the arrangement of various limiting structures and fixing structures can reduce the displacement or vibration of the truss bottom plate in the processing process, and ensure the accuracy of the processed finished product; the control screen can adjust various controllable parameters of the screw machine, and the processing range of the screw machine is expanded.
Drawings
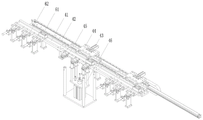
Fig. 1 is a schematic diagram of an embodiment of the present invention between transmission devices.
Fig. 2 is a front view of the embodiment.
Fig. 3 is a rear view structural diagram of the embodiment.
Fig. 4 is a schematic structural diagram of the stepping mechanism in the embodiment.
FIG. 5 is a front view of the processing mechanism in the embodiment.
Fig. 6 is a rear view structural schematic diagram of the processing mechanism in the embodiment.
FIG. 7 is a schematic view showing a structure of a punching apparatus in the embodiment.
Fig. 8 is a schematic structural view of the feeding mechanism in the embodiment.
Fig. 9 is a front view of the feeding mechanism in the embodiment.
Fig. 10 is a schematic structural view of a diaphragm portion in the embodiment.
FIG. 11 is a schematic diagram of the structure of the primary rail and the secondary rail in the embodiment.
The accompanying drawings, which are included to provide a further understanding of the application and are incorporated in and constitute a part of this application, illustrate embodiment(s) of the application and together with the description serve to explain the application and not to limit the application.
Detailed Description
In order to make the aforementioned objects, features and advantages of the present invention comprehensible, embodiments accompanied with figures are described in detail below.
Examples are given.
As shown in fig. 1 to 3, the present embodiment includes a base 1 disposed between a conveying device for conveying a truss base plate to be processed and a truss base plate that has been processed, and a stepping mechanism for stepping the truss base plate in the screw machine, a feeding mechanism for conveying a fixing base to be screwed to a designated processing place, and a processing mechanism for fixing the fixing base to the truss base plate are disposed on the base 1.
As shown in fig. 4, the provided stepping mechanism includes a stepping rail 21 fixed to the base 1, and a feeding end 211 and a discharging end 212 are respectively provided at two ends of the stepping rail 21, wherein one end of the feeding end 211 is connected to a transmission device for transmitting a truss bottom plate to be processed, and the discharging end 212 is connected to a transmission device for transmitting a truss bottom plate to be processed. Step pressing plate devices are arranged on two sides of the step rail 21, each step pressing plate device comprises a pressing plate rail 22 which is fixed with the base 1 and is parallel to the step rail 21, a movable pressing seat 23 which is arranged on the pressing plate rail 22 and can move along the pressing plate rail 22 under the drive of a motor, and a plurality of pressing plate cylinders 24 which are arranged on the movable pressing seat 23 at equal intervals, the pressing plate cylinders 24 are connected with the movable pressing seats 23 through a connecting structure which helps the pressing plate cylinders 24 to be closer to the step rail 21, the pressing plate cylinders 24 face the middle of the step rail 21 and are positioned above the edge of the step rail 21, step pressing plates 25 are fixed at the bottoms of the pressing plate cylinders 24, and the arranged step pressing plates 25 can move up and down in the vertical direction under the drive of the pressing plate cylinders 24. Specifically, after the truss bottom plate enters the stepping track 21 through the transmission device, the plurality of stepping press plates 25 move downwards to clamp the truss bottom plate, and then the movable press seats 23 move towards the direction of the discharge end 212 so as to drag the truss bottom plate to move on the stepping track 21; after the movable pressing seat 23 moves to one end of the pressing plate rail 22, the stepping pressing plate 25 moves upwards to release the truss bottom plate, the movable pressing seat 23 moves to the other end of the pressing plate rail 22 towards the direction of the feeding end 211, so that one stepping action of the truss bottom plate is completed, and the truss bottom plate can move in the stepping rail 21, namely the screw machine in such a cycle. In addition, the stepping track 21 is further provided with an inductive switch 20, and the inductive switch 20 is used for sensing the position of the bottom plate of the truss positioned in the stepping track 21 so as to facilitate subsequent processing.
In this embodiment, a limiting seat 26 parallel to the stepping rail 21 and each of the pressing plate rails 22 is further disposed between the stepping rail 21 and each of the pressing plate rails 22, a plurality of limiting rollers 261 are fixed on the limiting seat 26, positions of the limiting rollers 261 correspond to positions of the truss bottom plate, and the limiting rollers 261 are connected with two sides of the truss bottom plate when the truss bottom plate moves in the stepping rail 21, so that limitation of the truss bottom plate is achieved, and the roller structure can help the truss bottom plate to move more smoothly.
As shown in fig. 5 to 7, the processing mechanism includes a fixing frame 31 fixed to the base 1, a plurality of perforating devices 32 are arranged in a row on one side of the fixing frame 31 close to the feeding end 211, a screwing device 33 corresponding to the perforating device 32 is arranged on one side of the fixing frame 31 close to the discharging end 212, the perforating device 32 and the screwing device 33 are both located above the stepping track 21, the perforating device 32 is used for perforating on a truss bottom plate which is stepped to the lower side of the perforating device, and the screwing device 33 is used for fixing screws in the drilled holes after the perforation is completed. A screw feeder 34 is provided adjacent to the mounting bracket 31 and connected to each screw loading device 33, the screw feeder 34 being provided for guiding the screws to be used into the screw loading devices 33.
In this embodiment, one side of the fixing frame 31 close to the feeding end 211 is provided with a back-moving prevention device above the stepping track 21, and the back-moving prevention device is closer to the feeding end 211 than the punching device 32. The anti-retreat device comprises an anti-retreat cylinder 35 and a stop block 351 connected to the lower part of the anti-retreat cylinder 35, the stop block 351 is used for realizing the movement in the vertical direction through the anti-retreat cylinder 35, and when the stop block 351 moves downwards to press or abut against a truss bottom plate positioned below the stop block, the truss bottom plate can be prevented from moving during processing (including punching and screwing). The fixing frame 31 is provided with a feeding pressing plate device which is located between the anti-back device and the punching device 32 and above the stepping track 21 on one side close to the feeding end 211, the feeding pressing plate device comprises a punching cylinder 36 and a punching pressing plate 361 connected to the lower portion of the punching cylinder 36, the punching pressing plate 361 is moved in the vertical direction through the punching cylinder 36, and when the punching pressing plate 361 moves down to press the position beside a punching position on the truss bottom plate, punching errors caused by vibration of the truss bottom plate during punching can be prevented. In addition, the fixing frame 31 is provided with a discharging pressure plate device on the side close to the discharging end 212, the discharging pressure plate device comprises a screw cylinder 37 located beside the upper screw device 33 and a screw pressure plate 371 connected to the lower portion of the screw cylinder 37, the screw pressure plate 371 moves in the vertical direction through the screw cylinder 37, and when the screw pressure plate 371 moves down to press the position beside the punching position on the truss bottom plate, the punching error of the truss bottom plate caused by vibration during punching can be prevented.
As shown in fig. 8-11, the feeding structure includes a main rail 41 fixed on the base 1 and penetrating the lower portion of the stepping rail 21, and a sub-rail 42 fixed on the base 1 and parallel to the main rail 41. The two ends of the main rail 41 are symmetrically provided with vibration discs 51, the vibration discs 51 are connected with material placing grooves 52 opposite to the main rail 41, fixing seats to be fixed by screws are placed in the vibration discs 51, and the fixing seats can be sequentially sent into the material placing grooves 52 and simultaneously arranged in a row through the arranged vibration discs 51. A transfer device is arranged beside the material holding groove 52, and a plurality of moving jigs 61 which are matched with the transfer device and can move along the main track 41 are arranged on the main track 41. The provided transfer device comprises a transfer rail 53 which is fixed on the base 1 and is parallel to the main rail 41, and a lifting manipulator 54 which is arranged on the transfer rail 53 and is matched with the moving jig 61, wherein a clamping rod 55 is arranged at the bottom of the lifting manipulator 54, the lifting manipulator 54 can move along the transfer rail 53, the clamping rod 55 at the lower part of the lifting manipulator can move in the vertical direction, the clamping rod 55 can be inserted into the fixed seat to form clamping connection so as to move the fixed seat, and the clamping rod 55 is positioned right above the material placing groove 52 and the part of the main rail 41 close to one end of the material placing groove 52 along with the moving track of the lifting manipulator 54. The top of the movable jig 61 is inwards recessed to form a placing groove matched with the inverted fixing seat structure, specifically, the lifting manipulator 54 moves to one end close to the placing groove 52 on the transfer track 53, the clamping rod 55 moves downwards to clamp a fixing seat and then the lifter moves to one end close to the main track 41, the clamping rod 55 moves downwards to place the fixing seat in the placing groove and then moves upwards, and in this way, each fixing seat is repeatedly transferred to the movable jig 61 located on the designated position from the placing groove 52. The auxiliary rail 42 is provided with a pushing cylinder 43 capable of moving along the auxiliary rail 42, the pushing cylinder 43 is connected with a fixture 44 matched with the moving jig 61 towards one side of the main rail 41, specifically, after a fixed seat is placed in the moving jig 61 positioned at one end of the main rail 41, the fixture 44 moves towards the moving jig 61 under the driving of the pushing cylinder 43 until the fixture 44 is clamped with the moving jig 61 in the direction opposite to the main rail 41, then the pushing cylinder 43 moves towards the middle direction along the auxiliary rail 42, namely, the fixture 44 carries the moving jig 61 to move towards the middle position of the main rail 41 in the main rail 41 until the moving jig 61 reaches a specified position, the pushing cylinder 43 stops moving, and at this time, the moving jig 61 is positioned right below an upper screw device 33. The middle of the main rail 41 is provided with a movable structure 45 movably connected with the main rail 41 and located right below the screw-up device 33, a jig lifting device 46 connected with the movable structure 45 and fixed with the base 1 is arranged right below the movable structure 45, specifically, after the movable jig 61 is driven by the fixture 44 to move to the middle of the main rail 41, namely the movable structure 45, the jig lifting device 46 pushes the movable structure 45 upwards to drive the movable jig 61 located on the movable structure 45, so that the fixed seat placed in the movable jig 61 is connected with the lower surface of the truss bottom plate, thereby implementing the subsequent screw-up step, and after the fixation of the movable structure 45 and the movable structure 45 is completed, the jig lifting device 46 retracts to enable the movable structure 45 to return to the original state. In addition, the lower portion of the transfer rail 53 is provided with a positioning seat 62 matched with the fixture 44, when the fixture 44 moves towards the main rail 41, the fixture 44 is gradually folded with the positioning seat 62, so that the movable jig 61 is clamped, and when a plurality of movable jigs 61 are provided, the corresponding positioning seats 62 are matched with the fixture 44, so that the clamping efficiency of the fixture 44 can be improved.
In this embodiment, the number of the movable jigs 61 is three, three positions capable of clamping the movable jigs 61 are correspondingly arranged on the fixture 44, and three lifting manipulators 54 are arranged on each transfer rail 53, that is, the number of the transfer screws of each fixing seat is three. The vibration disc 51, the material placing groove 52 and the transfer device in the screw machine are symmetrically arranged, the vibration disc 51, the material placing groove 52 and the transfer device which are positioned at one end of the main rail 41 are correspondingly provided with a group of moving jigs 61 positioned on the main rail 41 and a pushing cylinder 43 positioned on the auxiliary rail 42, and particularly, when the moving jigs 61 positioned at one end of the main rail 41 are used for carrying out fixed seat transfer, the other group of moving jigs 61 are driven by the other end of the main rail 41 to move to the middle part of the main rail 41 with the fixed seats positioned in the placing groove to be fixed with screws of the truss bottom plate; when the movable jig 61 located at one end of the main rail 41 is driven by the fixture 44 to move towards the middle of the main rail 41 after completing the transfer of the fixing seat, the other group of movable jigs 61 is driven by the fixture 44 to move towards the other end of the main rail 41 for the next fixing seat transfer, and the feeding speed of the fixing seats can be increased by the circulation, so that the fixing processing efficiency of the truss bottom plate is improved.
In this embodiment, the fixing frame 31 is provided with a control panel 7 facing the feeding end 211, and the control panel 7 is connected to the stepping pressing device, the punching device 32, the screwing device 33, the transferring device, the pushing cylinder 43, and the inductive switch 20. The control screen 7 is used for controlling the working mode of the screw machine and adjusting various controllable parameters, such as the distance between the positions of the rows of fixing seats.
The invention provides a detachable truss screw machine which is scientific in structure, saves the manual process of feeding, realizes full automation of the machining process and is high in machining efficiency. Be provided with all kinds of limit structure and fixed knot and construct, can reduce the displacement or the condition of vibrations appear in the truss bottom plate in the course of working, guaranteed the accuracy of processing the finished product. The control screen 7 can adjust various controllable parameters of the screw machine, and the processing range of the screw machine is expanded.
The above description of the present invention is intended to be illustrative. Various modifications, additions and substitutions for the specific embodiments described may be made by those skilled in the art without departing from the scope of the invention as defined in the accompanying claims.
Claims (5)
1. Removable truss screw machine, including base and step mechanism, feeding mechanism and the processing agency of setting on the base, its characterized in that: the stepping mechanism comprises a stepping track fixed with the base and stepping pressure plate devices arranged on two sides of the stepping track, and the stepping track is provided with a feeding end and a discharging end; the stepping pressing plate device comprises a pressing plate rail fixed with the base, a movable pressing seat arranged on the pressing plate rail and capable of moving along the pressing plate rail, a plurality of pressing plate air cylinders arranged on the movable pressing seat and facing the stepping rail, and stepping pressing plates fixed on the pressing plate air cylinders; a limiting seat is arranged between the stepping track and the pressing plate track, and a plurality of limiting rollers are fixed on the limiting seat;
the processing mechanism comprises a fixed frame which is fixed with the base and is positioned above the stepping track, a punching device which is arranged on one side of the fixed frame towards the feeding end, a screw feeding device which is arranged on one side of the fixed frame towards the discharging end and corresponds to the punching device, and a screw feeding machine which is arranged beside the fixed frame and is connected with the screw feeding device;
the feeding structure comprises a main rail fixed on the base and penetrating through the lower part of the stepping rail and an auxiliary rail fixed on the base and parallel to the main rail, wherein vibration discs are symmetrically arranged at two ends of the main rail, a material placing groove opposite to the main rail is connected to the vibration discs, a corresponding transfer device is arranged beside the material placing groove, a plurality of moving jigs which are matched with the transfer device and can move along the main rail are arranged on the main rail, a pushing cylinder capable of moving along the auxiliary rail is arranged on the auxiliary rail, and a clamp matched with the moving jigs is connected to one side, facing the main rail, of the pushing cylinder;
The control screen facing the feeding end is arranged on the fixing frame and is respectively connected with the stepping pressing plate device, the punching device, the screw feeding device, the transferring device and the pushing cylinder;
the transferring device comprises a transferring track which is fixed on the base and is parallel to the main track, and a lifting manipulator which is arranged on the transferring track and is matched with the moving jig, wherein a clamping rod is arranged at the bottom of the lifting manipulator;
a positioning seat matched with the fixture is arranged at the lower part of the transfer track; the middle part of the main track is provided with a movable structure which is movably connected with the main track and is positioned right below the upper screw device, and a jig lifting device which is fixed with the movable structure is arranged right below the movable structure.
2. The removable truss screw machine of claim 1 wherein: the mount is provided with to feed end one side and prevents moving back the device, prevents moving back the device including preventing moving back the cylinder and connecting at the dog that prevents moving back the cylinder lower part.
3. The removable truss screw machine of claim 2, wherein: the mount is provided with the feeding presser device that is located between anti-moving back device and the perforating device to feed end one side, and feeding presser device is including the cylinder and the clamp plate of connecting in the cylinder lower part that punches of punching.
4. A detachable truss screw machine as defined in claim 1, 2 or 3 wherein: the fixing frame is provided with a discharge pressing plate device towards one side of the discharge end, and the discharge pressing plate device comprises a screw cylinder and a screw pressing plate, wherein the screw cylinder is positioned beside the upper screw device, and the screw pressing plate is connected to the lower portion of the screw cylinder.
5. The removable truss screw machine of claim 1, wherein: the stepping track is provided with an inductive switch connected with the control screen.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010506545.5A CN111644834B (en) | 2020-06-05 | 2020-06-05 | Detachable truss screw machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010506545.5A CN111644834B (en) | 2020-06-05 | 2020-06-05 | Detachable truss screw machine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN111644834A CN111644834A (en) | 2020-09-11 |
| CN111644834B true CN111644834B (en) | 2022-05-24 |
Family
ID=72350472
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010506545.5A Active CN111644834B (en) | 2020-06-05 | 2020-06-05 | Detachable truss screw machine |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111644834B (en) |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112475367B (en) * | 2020-11-23 | 2024-01-23 | 广州市瑞搏特自动化设备有限公司 | Drilling and screwing machine for hidden anti-theft net profile |
| CN113020653B (en) * | 2021-03-09 | 2022-10-28 | 山东七星绿色建筑科技有限公司 | Truss 3D floor board puncher |
| CN113059343B (en) * | 2021-04-13 | 2022-05-17 | 广东容宏科技有限公司 | Annular circulating mechanism for die assembly and screwing of tubular pile die |
| CN113530253B (en) * | 2021-08-10 | 2023-05-02 | 渝建建筑工业科技集团有限公司 | Semi-automatic steel bar truss building carrier plate assembly production line |
| CN113523822B (en) * | 2021-08-11 | 2022-06-21 | 渝建建筑工业集团有限公司 | Full-automatic production line for steel bar truss floor bearing plate |
| CN113547290B (en) * | 2021-08-11 | 2022-06-24 | 渝建建筑工业集团有限公司 | Novel full-automatic production line of steel bar truss floor carrier plate |
| CN114211236B (en) * | 2022-01-18 | 2023-04-28 | 山东光明园迪儿童家具科技有限公司 | Control system of automatic screw locking equipment |
| CN114871466A (en) * | 2022-05-05 | 2022-08-09 | 山东七星绿色建筑科技有限公司 | 3D truss floor board production line |
| CN116276010B (en) * | 2023-03-20 | 2025-09-16 | 浙江亿洲机械科技有限公司 | Full-automatic disassembly-free truss screw assembly machine |
| CN116460501B (en) * | 2023-04-04 | 2023-12-29 | 浙江亿洲机械科技有限公司 | Truss footing welding machine |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105178606A (en) * | 2015-08-07 | 2015-12-23 | 孟令启 | Automatic vibration device |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4562756A (en) * | 1983-07-19 | 1986-01-07 | Matsushita Electric Industrial Co., Ltd. | Numerical control screw tightening machine |
| CN204737393U (en) * | 2015-06-29 | 2015-11-04 | 惠州市德赛电池有限公司 | Automatic bat printing fastener tool loop structure |
| CN105797917B (en) * | 2016-05-20 | 2019-04-16 | 厦门力巨自动化科技有限公司 | Point glue adhering machine |
| CN107738093A (en) * | 2017-11-20 | 2018-02-27 | 东莞理工学院 | A heat sink automatic screw locking machine |
| CN208644595U (en) * | 2018-06-08 | 2019-03-26 | 浙江亿洲机械科技有限公司 | Screw automatic assembling machine |
| CN109500614A (en) * | 2018-11-27 | 2019-03-22 | 广东顶固集创家居股份有限公司 | Inserted sheet cylinder automatic processing device |
| CN109676375B (en) * | 2019-02-27 | 2023-03-14 | 河北诺舟自动化科技有限公司 | Full-automatic chain belt screw assembling machine |
-
2020
- 2020-06-05 CN CN202010506545.5A patent/CN111644834B/en active Active
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105178606A (en) * | 2015-08-07 | 2015-12-23 | 孟令启 | Automatic vibration device |
Also Published As
| Publication number | Publication date |
|---|---|
| CN111644834A (en) | 2020-09-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111644834A (en) | Detachable truss screw machine | |
| CN108568707B (en) | Truss floor carrier plate assembly production line | |
| CN108747413B (en) | Full-automatic flange processing assembly line | |
| CN103433585B (en) | The wheeled automatic brazing machine of a kind of Timing Belt | |
| CN218983623U (en) | PCB board laser marking board material conveyor | |
| CN112588938A (en) | Punching equipment for processing solar frame | |
| CN212552618U (en) | Detachable truss screw machine | |
| CN107253060B (en) | Full-automatic square hole machine for shaft | |
| CN106426423A (en) | Woodworking cutting and punching all-in-one machine | |
| CN116021484B (en) | Bed core and frame assembly device | |
| CN208644595U (en) | Screw automatic assembling machine | |
| CN203459787U (en) | Synchronous pulley type automatic soldering machine | |
| CN211136437U (en) | Automatic punching device for door and window material processing | |
| KR20160145445A (en) | Spacer automatic assembly device of form removal deck | |
| CN218285295U (en) | Bed core and frame assembling and positioning mechanism | |
| CN115383497B (en) | Automatic feeding slot pulling machine | |
| CN116276010B (en) | Full-automatic disassembly-free truss screw assembly machine | |
| CN211135609U (en) | A batch perforating device for door and window material | |
| CN108422526B (en) | Multi-truss wood truss assembling equipment | |
| CN210283574U (en) | A lifting mechanism applied to screen printing equipment | |
| CN110524209B (en) | Flexible finished product lamp strip positioning mechanism and lamp strip equipment on flexible full-compatible television | |
| CN210139082U (en) | A kind of fire door glass pressing frame installation hole drilling and forming equipment | |
| CN219445249U (en) | Substrate cutting equipment | |
| CN223833987U (en) | A universal positioning fixture for automatic loading and unloading of CNC machines | |
| CN220196831U (en) | Automatic jump ring assembly device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |