CN111590869A - Blow molding machine for processing PE (polyethylene) film - Google Patents
Blow molding machine for processing PE (polyethylene) film Download PDFInfo
- Publication number
- CN111590869A CN111590869A CN202010460954.6A CN202010460954A CN111590869A CN 111590869 A CN111590869 A CN 111590869A CN 202010460954 A CN202010460954 A CN 202010460954A CN 111590869 A CN111590869 A CN 111590869A
- Authority
- CN
- China
- Prior art keywords
- blow molding
- film
- pipe
- wind ring
- heating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- 238000000071 blow moulding Methods 0.000 title claims abstract description 62
- 239000004698 Polyethylene Substances 0.000 title description 18
- -1 polyethylene Polymers 0.000 title description 4
- 229920000573 polyethylene Polymers 0.000 title description 4
- 238000010438 heat treatment Methods 0.000 claims abstract description 71
- 238000007664 blowing Methods 0.000 claims abstract description 27
- 238000001816 cooling Methods 0.000 claims description 43
- 238000003466 welding Methods 0.000 claims description 11
- 238000004804 winding Methods 0.000 claims description 3
- 238000009434 installation Methods 0.000 claims description 2
- 229920000426 Microplastic Polymers 0.000 abstract description 8
- 238000005338 heat storage Methods 0.000 abstract description 8
- 238000002844 melting Methods 0.000 abstract description 5
- 230000008018 melting Effects 0.000 abstract description 5
- 238000001125 extrusion Methods 0.000 abstract description 2
- 238000003825 pressing Methods 0.000 description 14
- 239000004033 plastic Substances 0.000 description 13
- 229920003023 plastic Polymers 0.000 description 13
- 239000002245 particle Substances 0.000 description 12
- 238000004806 packaging method and process Methods 0.000 description 5
- 230000008901 benefit Effects 0.000 description 4
- 238000007599 discharging Methods 0.000 description 4
- 239000012528 membrane Substances 0.000 description 4
- 230000005484 gravity Effects 0.000 description 3
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 2
- 229910052802 copper Inorganic materials 0.000 description 2
- 239000010949 copper Substances 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 230000002349 favourable effect Effects 0.000 description 2
- 238000010096 film blowing Methods 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 230000007547 defect Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 239000012535 impurity Substances 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 230000035699 permeability Effects 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C55/00—Shaping by stretching, e.g. drawing through a die; Apparatus therefor
- B29C55/28—Shaping by stretching, e.g. drawing through a die; Apparatus therefor of blown tubular films, e.g. by inflation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C35/00—Heating, cooling or curing, e.g. crosslinking or vulcanising; Apparatus therefor
- B29C35/16—Cooling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C35/00—Heating, cooling or curing, e.g. crosslinking or vulcanising; Apparatus therefor
- B29C35/16—Cooling
- B29C2035/1658—Cooling using gas
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2023/00—Use of polyalkenes or derivatives thereof as moulding material
- B29K2023/04—Polymers of ethylene
- B29K2023/06—PE, i.e. polyethylene
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Health & Medical Sciences (AREA)
- Oral & Maxillofacial Surgery (AREA)
- Thermal Sciences (AREA)
- Blow-Moulding Or Thermoforming Of Plastics Or The Like (AREA)
Abstract
The invention discloses a blow molding machine for processing a PE film, which structurally comprises a blow molding box, a box door, a feeding pipe and a motor, wherein the box door is arranged on one side of the blow molding box in a matching way, the bottom of the feeding pipe is embedded and fixed on the upper surface of the blow molding box, and the motor is arranged above the blow molding box; the heating pipe heating makes the inside temperature in heat storage chamber rise, and through the heat-conducting plate with heat conduction to the cartridge heater inside, thereby melt plastic granules, it rotates to change the board heating pipe simultaneously, the heat that makes the cartridge heater inner wall is even, it leads to for melting completely to avoid plastic granules to be heated the inequality, plastic granules after the melting forms the bubble at the blowing bench of blowing under the blowing of blowing head, bubble bottom extrusion clamp plate makes the baffle open through the lifter that the vacuum tube upwards promotes to correspond this moment, the not clamp plate that the not equidimension bubble can extrude different positions makes different baffles open, avoid strikeing the bubble surface between the air current, in order to avoid leading to the PE film to warp.
Description
Technical Field
The invention relates to the field of film processing equipment, in particular to a blow molding machine for processing a PE film.
Background
The PE film, namely the polyethylene film, has the characteristic of small moisture resistance and moisture permeability, the film blowing machine is equipment for heating, melting and blowing PE plastic particles into the film, the PE film for food packaging is used for adding dried plastic particles into a blanking hopper in the processing process, then the plastic particles are pushed forwards by the thrust of a screw rod and are gradually melted by heating outside a charging barrel, the molten plastic is subjected to impurity removal through a machine head filter screen, and then is subjected to blowing, cooling, pressing through a herringbone plate into a food packaging bag and then winding on a traction roller.
At present, a blowing machine for processing a PE film is in a molten state when a film bubble formed by the blowing machine just leaves a film head, needs to be rapidly cooled and shaped, and when a film is cooled by an air ring, the air flow of the air ring blows out to a certain angle, so that the larger film bubble can be impacted by the air flow to enable the film bubble to shake, and the formed PE film deforms.
Disclosure of Invention
The invention provides a blow molding machine for processing a PE (polyethylene) film, aiming at the defects that a film bubble formed by a film blowing machine is in a molten state just after leaving a film head, needs to be rapidly cooled and shaped, and is subjected to air flow impact to cause the shaking phenomenon of the film bubble due to the fact that the air flow of an air ring blows out at a certain angle when the air ring cools the film, so that the formed film is deformed.
The invention is realized by the following technical scheme: a blow molding machine for processing films structurally comprises a blow molding box, a box door, a feeding pipe and a motor, wherein the box door is arranged on one side of the blow molding box in a matching way, the bottom of the charging pipe is embedded and fixed on the upper surface of the blow molding box, the motor is arranged above the blow molding box, the blow molding box comprises a heating cylinder, an air ring, a pressing plate, a traction roller and a discharging pipe, the heating cylinder is arranged in the blow molding box, the bottom of the wind ring is welded at the left upper end of the heating cylinder, and is embedded in the left inner wall of the blow molding box, the bottom of the pressure plate is welded on the upper surface of the wind ring, the traction roller is connected with the inner wall of the blow molding box through a bolt and is positioned at the right side of the top of the pressure plate, the discharging pipe penetrates through the upper wall of the blow molding box, and the top end of the discharging pipe is connected with the bottom of the charging pipe, meanwhile, the tail end of the heating cylinder is fixedly embedded at the top of the heating cylinder, the cross section of the heating cylinder is in a shape of two, and the gap at the upper end of the pressing plate is smaller than the gap at the lower end of the pressing plate.
Further say, the cartridge heater includes screw rod, pivot, belt, siphunculus, blow head, screw rod horizontal installation is inside the cartridge heater, the pivot runs through in the cartridge heater right side wall and is located the same axis with the screw rod through the clearance, the belt winding is at the pivot right-hand member and links to each other with the motor, the siphunculus inlays and locates inside the cartridge heater, the blow head is installed in the siphunculus bottom and is located under the wind ring, the belt drives the screw rod upper end and outwards rotates.
Furthermore, the heating cylinder is composed of a heat conducting plate, a heating pipe, a fixing bolt and a shell cover, wherein the heat conducting plate and the screw rod are located on the same axis, the heating pipe is embedded and fixed on the outer surface of the heat conducting plate, the fixing bolt is connected to the turning position of the heating pipe through welding, the fixing bolt is pressed against the inner wall of the shell cover, the heating pipe is bent back and forth, and the heat conducting plate is a metal plate.
Furthermore, the heating pipe includes connecting rod, heat storage chamber, commentaries on classics board, the connecting rod welding is in the heating pipe left and right sides, the heat storage chamber is located the heating pipe all around, change board left side and connecting rod right-hand member and weld mutually, and change inboard the welding of board and at the pivot surface, the connecting rod is the copper pipe, and changes board right side cross section and be circular.
Furthermore, the air ring comprises a clamping block, a cooling plate, a supporting tube and a blow molding table, wherein the clamping block is fixedly embedded in the inner side of the air ring, the left side and the right side of the cooling plate are welded with the clamping block, the supporting tube is fixedly embedded in the cooling plate, the blow molding table is embedded in the air ring and is positioned on the same axis with the air ring, the cross section of the blow molding table is trapezoidal, and the diameter of the upper end of the blow molding table is larger than that of the lower end of the blow molding table.
Further say that, the cooling plate includes runner, cooling hole, clamp plate, the runner passes through gap connection in the cooling plate outside, the cooling hole inlays to be located inside the cooling plate, the clamp plate inlays to be located the cooling plate inboard and be located blow molding platform outer wall department, the runner has six, and the cooling hole is annular evenly distributed with the clamp plate.
Furthermore, the cooling hole includes hinge, baffle, lifter, vacuum tube, the hinge passes through bolted connection in the right wall on the cooling hole, the baffle is installed in the hinge left side, the lifter top is connected in baffle bottom and the other end through movable block in the vacuum tube left end through welded connection, the vacuum tube inlays and locates cooling hole bottom inner wall and right-hand member and cooperatees with the clamp plate, the big right-hand member of cooling hole left end is little, and the baffle equals with the gravity of clamp plate with the gravity that the lifter was closed.
Advantageous effects
Compared with the prior art, the blow molding machine for processing the film has the following advantages:
1. the invention has the beneficial effects that: inside adding the cartridge heater with plastic granules, drive the pivot through the belt and rotate, the pivot rotates and drives the screw rod and rotate and make the screw rod pass plastic granules forward, and the heating pipe heating makes the temperature of heat storage intracavity portion rise to inside with heat conduction to the cartridge heater through the heat-conducting plate, thereby melt plastic granules, change the board heating pipe simultaneously and rotate, make the heat of cartridge heater inner wall even, avoid plastic granules to be heated the inequality and lead to melting for complete.
2. The invention has the beneficial effects that: the plastic granules after melting blow at the blowing head down at the blowing bench form the membrane bubble, and the membrane bubble bottom extrusion clamp plate makes the baffle open through the lifter that the vacuum tube upwards promoted to correspond this moment, and the not clamp plate that the membrane bubble of equidimension can extrude different positions makes different baffles open, avoids strikeing the membrane bubble surface between the air current to lead to the PE film to warp.
Drawings
Other features, objects and advantages of the invention will become more apparent upon reading of the detailed description of non-limiting embodiments with reference to the following drawings:
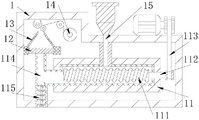
FIG. 1 is a schematic structural diagram of a blow molding machine for processing PE films according to the present invention.
FIG. 2 is an enlarged internal view of the blow molded case of the present invention.
FIG. 3 is a side view, cross-sectional view, enlarged, of the cartridge heater of the present invention.
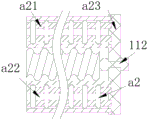
Fig. 4 is a schematic sectional enlarged view of the cartridge heater of the present invention.
FIG. 5 is a schematic view of an enlarged cross-sectional structure of the wind ring of the present invention.
Fig. 6 is a schematic top enlarged view of the wind ring of the present invention.
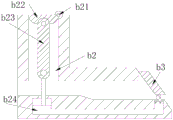
Fig. 7 is a cross-sectional enlarged view schematically illustrating a cooling plate according to the present invention.
In the figure: the blowing box comprises a blowing box 1, a box door 2, a feeding pipe 3, a motor 4, a heating cylinder 11, an air ring 12, a pressing plate 13, a traction roller 14, a blanking pipe 15, a screw 111, a rotating shaft 112, a belt 113, a through pipe 114, a blowing head 115, a heat conducting plate a1, a heating pipe a2, a fixing bolt a3, a shell cover a4, a connecting rod a21, a heat storage cavity a22, a rotating plate a23, a clamping block 121, a cooling plate 122, a supporting pipe 123, a blowing platform 124, a rotating wheel b1, a cooling hole b2, a pressing plate b3, a hinge b21, a baffle b22, a lifting rod b23 and a vacuum pipe b 24.
Detailed Description
In order to make the technical means, the original characteristics, the achieved purposes and the effects of the invention easy to understand, the following description and the accompanying drawings further illustrate the preferred embodiments of the invention.
Example 1:
please refer to fig. 1-4:
the invention provides a blow molding machine for processing PE films, which structurally comprises a blow molding box 1, a box door 2, a feeding pipe 3 and a motor 4, wherein the box door 2 is arranged on one side of the blow molding box 1 in a matching manner, the bottom of the feeding pipe 3 is embedded and fixed on the upper surface of the blow molding box 1, the motor 4 is arranged above the blow molding box 1, the blow molding box 1 comprises a heating cylinder 11, a wind ring 12, a pressure plate 13, a traction roller 14 and a blanking pipe 15, the heating cylinder 11 is arranged in the blow molding box 1, the bottom of the wind ring 12 is welded at the left upper end of the heating cylinder 11 and embedded and fixed on the left inner wall of the blow molding box 1, the bottom of the pressure plate 13 is welded on the upper surface of the wind ring 12, the traction roller 14 is connected to the inner wall of the blow molding box 1 through a bolt and positioned at the right of the top of the pressure plate 13, the blanking pipe 15 penetrates through the, the cross section of the heating cylinder 11 is T-shaped, two pressing plates 13 are arranged, and the gap at the upper end of each pressing plate 13 is smaller than that at the lower end, so that the blown film bubble can be fixed and pressed into a food packaging bag.
In the figure, the heating cylinder 11 includes a screw 111, a rotating shaft 112, a belt 113, a through pipe 114 and a blow head 115, the screw 111 is horizontally installed inside the heating cylinder 11, the rotating shaft 112 penetrates through the right wall of the heating cylinder 11 through a gap and is located on the same axis with the screw 111, the belt 113 is wound at the right end of the rotating shaft 112 and is connected with a motor, the through pipe 114 is embedded inside the heating cylinder 11, the blow head 115 is installed at the bottom of the through pipe 114 and is located under the wind ring 12, the belt 113 drives the upper end of the screw 111 to rotate outwards, and the screw 111 is favorable for pushing plastic particles forwards.
In the figure, the heating cylinder 11 is composed of a heat conducting plate a1, a heating tube a2, a fixing bolt a3 and a housing cover a4, the heat conducting plate a1 and the screw 111 are located on the same axis, the heating tube a2 is embedded on the outer surface of the heat conducting plate a1, the fixing bolt a3 is connected to the turning position of the heating tube a2 through welding, the fixing bolt a3 is resisted on the inner wall of the housing cover a4, the heating tube a2 is bent back and forth, and the heat conducting plate a1 is a metal plate, so that the temperature generated by the heating tube a2 is favorably transmitted into the heating cylinder 11 to melt plastic particles.
In the figure, heating pipe a2 includes connecting rod a21, heat storage chamber a22, commentaries on classics board a23, connecting rod a21 welds in the heating pipe a2 left and right sides, heat storage chamber a22 is located around heating pipe a2, commentaries on classics board a23 left side and connecting rod a21 right-hand member weld mutually, and commentaries on classics board a23 inboard welding in pivot 112 surface, connecting rod a21 is the copper pipe, and commentaries on classics board a23 right side cross-section is circular, does benefit to commentaries on classics board a23 and drives connecting rod a21 and heating pipe a2 and rotate at heating cylinder 11 inside, makes the heat of heating cylinder 11 inner wall even.
The specific principle of the embodiment is as follows: plastic particles are added into the heating cylinder 11 through the feeding pipe 3 and the discharging pipe 15, the starting motor 4 drives the rotating shaft 112 to rotate through the belt 113, the rotating shaft 112 drives the screw rod 111 to rotate, the screw rod 111 pushes the plastic particles forward, the heating pipe a2 on the inner wall of the heating cylinder 11 heats, the temperature inside the heat storage cavity a22 is raised, the heat is conducted to the inside of the heating cylinder 11 through the heat conducting plate a1, meanwhile, the rotating plate a23 drives the connecting rod a21 and the heating pipe a2 to rotate inside the heating cylinder 11, the heat on the inner wall of the heating cylinder 11 is uniform, the plastic particles are melted, the melted plastic particles flow to the through pipe 114, and at the moment, the plastic particles pass through the air ring 12 under the upward blowing of the blowing head 115 to form a film bubble and are cooled, a food packaging bag is formed at the pressing plate 13, and then the.
Example 2:
please refer to fig. 5-7:
the invention provides a blow molding machine for processing PE films, which structurally comprises a blow molding box 1, a box door 2, a feeding pipe 3 and a motor 4, wherein the box door 2 is arranged on one side of the blow molding box 1 in a matching manner, the bottom of the feeding pipe 3 is embedded and fixed on the upper surface of the blow molding box 1, the motor 4 is arranged above the blow molding box 1, the blow molding box 1 comprises a heating cylinder 11, a wind ring 12, a pressure plate 13, a traction roller 14 and a blanking pipe 15, the heating cylinder 11 is arranged in the blow molding box 1, the bottom of the wind ring 12 is welded at the left upper end of the heating cylinder 11 and embedded and fixed on the left inner wall of the blow molding box 1, the bottom of the pressure plate 13 is welded on the upper surface of the wind ring 12, the traction roller 14 is connected to the inner wall of the blow molding box 1 through a bolt and positioned at the right of the top of the pressure plate 13, the blanking pipe 15 penetrates through the, the cross section of the heating cylinder 11 is T-shaped, two pressing plates 13 are arranged, and the gap at the upper end of each pressing plate 13 is smaller than that at the lower end, so that the blown film bubble can be fixed and pressed into a food packaging bag.
In the figure, the heating cylinder 11 includes a screw 111, a rotating shaft 112, a belt 113, a through pipe 114 and a blow head 115, the screw 111 is horizontally installed inside the heating cylinder 11, the rotating shaft 112 penetrates through the right wall of the heating cylinder 11 through a gap and is located on the same axis with the screw 111, the belt 113 is wound at the right end of the rotating shaft 112 and is connected with a motor, the through pipe 114 is embedded inside the heating cylinder 11, the blow head 115 is installed at the bottom of the through pipe 114 and is located under the wind ring 12, the belt 113 drives the upper end of the screw 111 to rotate outwards, and the screw 111 is favorable for pushing plastic particles forwards.
In the drawing, the wind ring 12 includes a clamping block 121, a cooling plate 122, a supporting tube 123 and a blowing table 124, the clamping block 121 is embedded inside the wind ring 12, the left and right sides of the cooling plate 122 are welded to the clamping block 121, the supporting tube 123 is embedded inside the cooling plate 122, the blowing table 124 is embedded inside the wind ring 12 and located on the same axis with the wind ring 12, the cross section of the blowing table 124 is trapezoidal, and the diameter of the upper end of the blowing table 124 is large, the diameter of the lower end of the blowing table 124 is small, so that the blowing head 115 can blow the film to form the film bubble from bottom to top.
In the drawing, the cooling plate 122 includes runner b1, cooling hole b2, clamp plate b3, runner b1 passes through gap connection in the cooling plate 122 outside, cooling hole b2 inlays and locates inside the cooling plate 122, clamp plate b3 inlays and locates the inboard of cooling plate 122 and be located the outer wall department of blowing platform 124, runner b1 has six, and cooling hole b2 and clamp plate b3 are annular evenly distributed, do benefit to runner b1 and drive the cooling plate 122 and rotate at wind ring 12 inboard and carry out the cooling of blowing through cooling hole b2 to the film bubble.
In the figure, the cooling hole b2 comprises a hinge b21, a baffle b22, a lifting rod b23 and a vacuum tube b24, the hinge b21 is connected to the upper right wall of the cooling hole b2 through bolts, the baffle b22 is installed on the left side of the hinge b21, the top end of the lifting rod b23 is connected to the bottom of the baffle b22 through welding, the other end of the lifting rod b23 is connected to the left end of the vacuum tube b24 through movable clamping, the vacuum tube b24 is embedded in the inner wall of the bottom of the cooling hole b2, the right end of the cooling hole b2 is matched with a pressure plate b3, the left end of the cooling hole b2 is large and the right end of the cooling hole b2 is small, the combined gravity of the baffle b22 and the lifting rod b23 is equal.
The specific principle of the embodiment is as follows: the melted plastic particles pass through the air ring 12 under the blowing of the blow molding head 115 to form a film bubble on the blow molding table 124, at the moment, the bottom of the film bubble extrudes the pressing plate b3, the pressing plate b3 pushes the corresponding lifting rod b23 upwards through the vacuum tube b24, the lifting rod b23 drives the baffle b22 to open around the hinge b21, meanwhile, the rotating wheel b1 drives the cooling plate 122 to rotate on the inner side of the air ring 12 and carries out air blowing cooling on the film bubble through the cooling hole b2, the film bubbles with different sizes can extrude the pressing plates b3 at different positions to open different baffles b22, the surface of the film bubble is prevented from being impacted between air flows, and the PE film is prevented from being deformed.
The technical features of the embodiments described above may be arbitrarily combined, and for the sake of brevity, all possible combinations of the technical features in the embodiments described above are not described, but should be considered as being within the scope of the present specification as long as there is no contradiction between the combinations of the technical features.
Claims (5)
1. The utility model provides a blowing machine is used in processing of PE film, its structure includes blow molding case (1), chamber door (2), filling tube (3), motor (4), install in blow molding case (1) one side in chamber door (2) cooperation, filling tube (3) bottom inlays admittedly in blow molding case (1) upper surface, install in blow molding case (1) top motor (4), its characterized in that:
blow molding case (1) is including cartridge heater (11), wind ring (12), clamp plate (13), carry over pinch rolls (14), unloading pipe (15), install inside blow molding case (1) cartridge heater (11), wind ring (12) bottom welding is at cartridge heater (11) upper left end, and builds in blow molding case (1) left side inner wall, clamp plate (13) bottom welding is at wind ring (12) upper surface, carry over pinch rolls (14) through bolted connection in blow molding case (1) inner wall and be located clamp plate (13) top right-hand, unloading pipe (15) run through blow molding case (1) upper wall, and the top is connected in filling tube (3) bottom, and terminal simultaneously inlays admittedly in cartridge heater (11) top.
2. The blow molding machine for processing a PE film according to claim 1, wherein: heating cylinder (11) include screw rod (111), pivot (112), belt (113), siphunculus (114), blow head (115), screw rod (111) horizontal installation is inside heating cylinder (11), pivot (112) run through in heating cylinder (11) right side wall through the clearance and lie in the same axis with screw rod (111), belt (113) winding is at pivot (112) right-hand member and links to each other with the motor, siphunculus (114) are inlayed and are located heating cylinder (11) inside, blow head (115) are installed in siphunculus (114) bottom and are located under wind ring (12).
3. The blow molding machine for processing a PE film according to claim 1, wherein: the heating cylinder (11) is composed of a heat conducting plate (a1), a heating pipe (a2), a fixing bolt (a3) and a shell cover (a4), wherein the heat conducting plate (a1) and the screw (111) are located on the same axis, the heating pipe (a2) is embedded and fixed on the outer surface of the heat conducting plate (a1), the fixing bolt (a3) is connected to the turning position of the heating pipe (a2) through welding, and the fixing bolt (a3) is resisted on the inner wall of the shell cover (a 4).
4. The blow molding machine for processing a PE film according to claim 3, wherein: heating pipe (a2) includes connecting rod (a21), heat-retaining chamber (a22), commentaries on classics board (a23), connecting rod (a21) welding is in heating pipe (a2) left and right sides, heat-retaining chamber (a22) are located heating pipe (a2) all around, commentaries on classics board (a23) left side and connecting rod (a21) right-hand member weld mutually, and commentaries on classics board (a23) inboard welding is on pivot (112) surface.
5. The blow molding machine for processing a PE film according to claim 1, wherein: the wind ring (12) comprises a clamping block (121), a cooling plate (122), a supporting tube (123) and a blow molding table (124), the clamping block (121) is fixedly embedded in the inner side of the wind ring (12), the left side and the right side of the cooling plate (122) are welded with the clamping block (121), the supporting tube (123) is fixedly embedded in the cooling plate (122), and the blow molding table (124) is embedded in the wind ring (12) and is located on the same axis with the wind ring (12).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010460954.6A CN111590869A (en) | 2020-05-27 | 2020-05-27 | Blow molding machine for processing PE (polyethylene) film |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010460954.6A CN111590869A (en) | 2020-05-27 | 2020-05-27 | Blow molding machine for processing PE (polyethylene) film |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111590869A true CN111590869A (en) | 2020-08-28 |
Family
ID=72181652
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010460954.6A Pending CN111590869A (en) | 2020-05-27 | 2020-05-27 | Blow molding machine for processing PE (polyethylene) film |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111590869A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN118991016A (en) * | 2024-10-23 | 2024-11-22 | 晋江市民富鞋材有限公司 | Blow molding machine for PE film processing |
Citations (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20130000837A1 (en) * | 2011-06-29 | 2013-01-03 | Samsung Mobile Display Co., Ltd. | Substrate sealing apparatus and method of sealing substrate using the same |
| CN106113477A (en) * | 2016-06-29 | 2016-11-16 | 浙江汇锋薄膜科技有限公司 | A kind of plastic sheeting process equipment |
| CN206011717U (en) * | 2016-08-31 | 2017-03-15 | 瑞安市泓博塑业有限公司 | What a kind of film production was special prevents the inflation film manufacturing machine of film fold |
| CN209095961U (en) * | 2018-11-30 | 2019-07-12 | 潍坊中荷数高分子材料有限公司 | A kind of efficient PE thin film extruding machine |
| CN209756063U (en) * | 2019-03-08 | 2019-12-10 | 驻马店市中远塑胶有限公司 | A kind of air ring cooling blow molding device for polymer plastic film production |
| CN209888135U (en) * | 2019-01-02 | 2020-01-03 | 重庆亿恒包装有限公司 | Material heating device for blow molding machine |
| CN210100660U (en) * | 2018-10-31 | 2020-02-21 | 保定华标塑料制品有限公司 | Film blowing machine preheats compounding device |
| CN210123161U (en) * | 2019-04-24 | 2020-03-03 | 泰安亿润科技发展有限公司 | Novel be used for environmental protection granulator waste gas to burn heat retrieval and utilization device |
| CN110936594A (en) * | 2019-12-05 | 2020-03-31 | 黄海山 | Blow molding machine for processing PE (polyethylene) film |
| CN210552928U (en) * | 2019-08-02 | 2020-05-19 | 玉田县帅辰塑料制品有限公司 | Electromagnetic heating device of plastic extruder |
| CN210552930U (en) * | 2019-06-05 | 2020-05-19 | 绍兴海景塑业有限公司 | PE material processing equipment is used in processing of cosmetic bottle lid |
| CN210590476U (en) * | 2019-09-23 | 2020-05-22 | 四川长河塑业有限公司 | Extrusion film blowing device for PE (polyethylene) protective film |
-
2020
- 2020-05-27 CN CN202010460954.6A patent/CN111590869A/en active Pending
Patent Citations (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20130000837A1 (en) * | 2011-06-29 | 2013-01-03 | Samsung Mobile Display Co., Ltd. | Substrate sealing apparatus and method of sealing substrate using the same |
| CN106113477A (en) * | 2016-06-29 | 2016-11-16 | 浙江汇锋薄膜科技有限公司 | A kind of plastic sheeting process equipment |
| CN206011717U (en) * | 2016-08-31 | 2017-03-15 | 瑞安市泓博塑业有限公司 | What a kind of film production was special prevents the inflation film manufacturing machine of film fold |
| CN210100660U (en) * | 2018-10-31 | 2020-02-21 | 保定华标塑料制品有限公司 | Film blowing machine preheats compounding device |
| CN209095961U (en) * | 2018-11-30 | 2019-07-12 | 潍坊中荷数高分子材料有限公司 | A kind of efficient PE thin film extruding machine |
| CN209888135U (en) * | 2019-01-02 | 2020-01-03 | 重庆亿恒包装有限公司 | Material heating device for blow molding machine |
| CN209756063U (en) * | 2019-03-08 | 2019-12-10 | 驻马店市中远塑胶有限公司 | A kind of air ring cooling blow molding device for polymer plastic film production |
| CN210123161U (en) * | 2019-04-24 | 2020-03-03 | 泰安亿润科技发展有限公司 | Novel be used for environmental protection granulator waste gas to burn heat retrieval and utilization device |
| CN210552930U (en) * | 2019-06-05 | 2020-05-19 | 绍兴海景塑业有限公司 | PE material processing equipment is used in processing of cosmetic bottle lid |
| CN210552928U (en) * | 2019-08-02 | 2020-05-19 | 玉田县帅辰塑料制品有限公司 | Electromagnetic heating device of plastic extruder |
| CN210590476U (en) * | 2019-09-23 | 2020-05-22 | 四川长河塑业有限公司 | Extrusion film blowing device for PE (polyethylene) protective film |
| CN110936594A (en) * | 2019-12-05 | 2020-03-31 | 黄海山 | Blow molding machine for processing PE (polyethylene) film |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN118991016A (en) * | 2024-10-23 | 2024-11-22 | 晋江市民富鞋材有限公司 | Blow molding machine for PE film processing |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN113459457A (en) | Preparation facilities of HDPE tubular product | |
| CN110917992A (en) | A granulation equipment for feed production | |
| CN211074663U (en) | Plastic film blowing machine | |
| CN211165209U (en) | Blow molding equipment for CPP film packaging material | |
| CN220517492U (en) | Extrusion molding equipment based on protection bag production | |
| CN118082152B (en) | Thermoplastic die device for PVC production | |
| CN113199694A (en) | Automatic change injection mold molding machine | |
| CN206870342U (en) | A kind of multi-layered composite pipe extruder | |
| CN214137319U (en) | Prevent blown film equipment of static | |
| CN210590476U (en) | Extrusion film blowing device for PE (polyethylene) protective film | |
| CN213593475U (en) | Electric injection device of injection molding machine | |
| CN206464717U (en) | A kind of PE welds the production equipment of bar | |
| CN112660512B (en) | Automatic wrapping method and device | |
| CN220095168U (en) | Drying device | |
| CN114536646A (en) | Electric smelting pipe fitting wire winding drawing of patterns all-in-one | |
| CN101972838A (en) | Continuous casting production line | |
| CN217047481U (en) | Wrapping bag blown film device | |
| CN119502207A (en) | Rotational molding device and method | |
| CN210336543U (en) | Plastic melting device | |
| CN205851858U (en) | Wheel hub casting machine | |
| CN223618207U (en) | Recycled plastic forming device | |
| CN217293381U (en) | Integrative injection mold of new energy automobile power plug | |
| CN207594133U (en) | A kind of injection moulding machine | |
| CN214645775U (en) | Dryer for extruder | |
| CN214491516U (en) | Extruder is used in cable processing |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination |