CN111572881A - A fully automatic packing machine - Google Patents
A fully automatic packing machine Download PDFInfo
- Publication number
- CN111572881A CN111572881A CN202010380929.7A CN202010380929A CN111572881A CN 111572881 A CN111572881 A CN 111572881A CN 202010380929 A CN202010380929 A CN 202010380929A CN 111572881 A CN111572881 A CN 111572881A
- Authority
- CN
- China
- Prior art keywords
- conveying roller
- gripper
- vertical
- roller way
- baffle
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000012856 packing Methods 0.000 title description 14
- 239000007788 liquid Substances 0.000 claims abstract description 41
- 230000000712 assembly Effects 0.000 claims description 7
- 238000000429 assembly Methods 0.000 claims description 7
- 238000012423 maintenance Methods 0.000 abstract description 3
- 238000010586 diagram Methods 0.000 description 4
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000004806 packaging method and process Methods 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/52—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation using roller-ways or endless conveyors
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/10—Feeding, e.g. conveying, single articles
- B65B35/22—Feeding, e.g. conveying, single articles by roller-ways
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/10—Filling containers or receptacles progressively or in stages by introducing successive articles, or layers of articles
- B65B5/105—Filling containers or receptacles progressively or in stages by introducing successive articles, or layers of articles by grippers
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Microelectronics & Electronic Packaging (AREA)
- Container Filling Or Packaging Operations (AREA)
- Basic Packing Technique (AREA)
Abstract
Description
技术领域technical field
本发明涉及机械领域,尤其涉及一种全自动装箱机。The invention relates to the field of machinery, in particular to a fully automatic case packing machine.
背景技术Background technique
随着人工成本越来越高,各种依靠流水线生产劳动密集型企业压力日益增加,以自动化设备代替人力已经成为趋势,其中以有关机器人的全自动设备备受青睐。其中包括码垛、装箱、开箱、焊接等各方面的应用。As labor costs are getting higher and higher, various labor-intensive enterprises relying on assembly line production are under increasing pressure, and it has become a trend to replace manpower with automated equipment. Among them, fully automatic equipment related to robots is favored. These include palletizing, packing, unpacking, welding and other applications.
液袋装箱一直是包装机械一个难题,特别是冷冻软袋食品,表面湿滑,用一般的抓取式抓手容易掉落,而且容易造成软袋损坏,装箱定位不准,而且不能兼容多种规格的软袋。如果用人工装箱则每条线的装箱部分需要6人/天,耗时耗力容易出错,且卫生状况需要得到特别的管理,卫生风险高。Liquid bag packing has always been a difficult problem for packaging machinery, especially frozen soft bag food. The surface is wet and slippery. It is easy to fall off with a general grabbing handle, and it is easy to cause damage to the soft bag, inaccurate packing positioning, and incompatibility. Various sizes of soft bags. If manual packing is used, the packing part of each line requires 6 people/day, which is time-consuming and labor-intensive and prone to errors. Moreover, the sanitation needs to be specially managed, and the sanitation risk is high.
发明内容SUMMARY OF THE INVENTION
本发明的目的是提供 一种全自动装箱机。The purpose of the present invention is to provide a fully automatic case packing machine.
本发明的创新点在于本发明中的全自动装箱机工作效率高、定位准确、运行平稳、噪音小、不会损坏纸箱和液袋、易调节、方便后期维护。The innovative point of the present invention is that the automatic case packing machine in the present invention has high working efficiency, accurate positioning, stable operation, low noise, no damage to cartons and liquid bags, easy adjustment and convenient later maintenance.
为实现上述发明目的,本发明的技术方案是:一种全自动装箱机,包括机架、液袋输送辊道、液袋抓手、纸箱输送辊道,所述纸箱输送辊道和液袋输送辊道垂直且存在间距,所述液袋抓手位于纸箱输送辊道和液袋输送辊道之间并位于液袋输送辊道的输出端端部;所述液袋抓手包括两平行布置的抓手组件,抓手组件包括竖直布置的支架、抓手,所述抓手包括一横杆和若干并列布置在横杆上的抓杆,抓手的横杆与支架铰链,支架上还设有水平布置的抓手气缸,抓手气缸的活塞杆端部连接一直齿条,支架上设有一水平布置的扇形齿条滑动杆,扇形齿条滑动杆上设有一和直齿条齿合的扇形齿条,扇形齿条上设有扇形通孔,扇形齿条滑动杆穿过扇形通孔并和扇形齿条板面方向垂直,扇形齿条通过连接杆和横杆连接,连接杆为扇形齿条的半径,抓杆位于水平状态时,两抓手组件的抓杆交错排列,两抓手组件上方设有水平直线滑轨,水平直线滑轨中部设有支撑板将水平直线滑轨分隔为两段,两段上均设有滑块,所述两抓手组件分别设置在两滑块上,抓手组件的支架顶部和滑块底部连接,支撑板上设有两水平布置的滑块气缸分别和两滑块连接;所述液袋抓手通过移动组件和机架相连,所述移动组件包括竖向移动机构和水平移动机构,水平直线滑轨两端连接在竖向移动机构上,竖向移动机构连接在水平移动机构上,水平移动机构位于纸箱输送辊道及纸箱输送辊道和液袋输送辊道的间距上方,水平移动机构的移动方向和液袋输送辊道的输送方向一致。In order to achieve the above purpose of the invention, the technical scheme of the present invention is: a fully automatic cartoning machine, comprising a frame, a liquid bag conveying roller table, a liquid bag gripper, a carton conveying roller table, the carton conveying roller table and the liquid bag The conveying roller table is vertical and there is a gap, and the liquid bag gripper is located between the carton conveying roller table and the liquid bag conveying roller table and is located at the output end of the liquid bag conveying roller table; the liquid bag gripper includes two parallel arrangements The gripper assembly includes a vertically arranged bracket and a gripper, the gripper includes a horizontal bar and a plurality of gripping bars arranged in parallel on the horizontal bar, the horizontal bar of the gripper is hinged with the bracket, and the bracket is also There is a horizontally arranged gripper cylinder, the end of the piston rod of the gripper cylinder is connected with a straight rack, the bracket is provided with a horizontally arranged sector rack sliding rod, and the sector rack sliding rod is provided with a straight rack gear. Fan-shaped rack, the fan-shaped rack is provided with a fan-shaped through hole, the fan-shaped rack sliding rod passes through the fan-shaped through hole and is perpendicular to the direction of the fan-shaped rack plate, the fan-shaped rack is connected by a connecting rod and a cross rod, and the connecting rod is a fan-shaped tooth The radius of the bar, when the grab bar is in a horizontal state, the grab bars of the two gripper assemblies are arranged in a staggered manner, a horizontal linear slide rail is arranged above the two gripper assemblies, and a support plate is arranged in the middle of the horizontal linear slide rail to separate the horizontal linear slide rail into two parts. The two sections are provided with sliders, the two gripper assemblies are respectively arranged on the two sliders, the top of the bracket of the gripper assembly is connected with the bottom of the slider, and the support plate is provided with two horizontally arranged slider cylinders respectively connected with two sliding blocks; the liquid bag gripper is connected with the frame through a moving assembly, the moving assembly includes a vertical moving mechanism and a horizontal moving mechanism, the two ends of the horizontal linear slide rail are connected to the vertical moving mechanism, and the vertical moving mechanism The moving mechanism is connected to the horizontal moving mechanism, and the horizontal moving mechanism is located above the distance between the carton conveying rollers and the carton conveying rollers and the liquid bag conveying rollers. The moving direction of the horizontal moving mechanism is consistent with the conveying direction of the liquid bag conveying rollers.
进一步地,所述水平移动机构包括两平行布置的水平环形链条组以及驱动水平环形链条组上的水平环形链条转动的驱动电机;所述竖向移动机构包括位于水平环形链条上的竖直布置的竖直侧板,竖直侧板上设有竖直滑轨及竖直环形链条组以及驱动竖直环形链条组的竖直环形链条转动的驱动电机,竖直滑轨上设有在竖直滑轨上滑动的竖直滑板,竖直滑板背面和竖直环形链条组的竖直环形链条相连,抓手的水平直线滑轨的两端分别和两竖直侧板上的竖直滑板连接。Further, the horizontal moving mechanism includes two horizontal annular chain groups arranged in parallel and a drive motor for driving the horizontal annular chain on the horizontal annular chain group to rotate; the vertical moving mechanism includes a vertically arranged chain on the horizontal annular chain. Vertical side plate, the vertical side plate is provided with a vertical slide rail, a vertical ring chain group and a driving motor for driving the vertical ring chain of the vertical ring chain group to rotate, and the vertical slide rail is provided with a vertical slide rail. For the vertical sliding plate sliding on the rail, the back of the vertical sliding plate is connected with the vertical annular chain of the vertical annular chain group, and the two ends of the horizontal linear sliding rail of the gripper are respectively connected with the vertical sliding plates on the two vertical side plates.
进一步地,所述纸箱输送辊道上设有一号挡板、二号挡板、三号挡板,所述一号挡板、二号挡板、三号挡板从纸箱输送辊道的输入端至输出端方向依次布置,所述一号挡板、三号挡板均通过一号挡板气缸推动,一号挡板气缸的伸缩方向和纸箱输送辊道输送方向垂直,二号挡板包括一号板和二号板,一号板和二号板之间存在夹角,一号板和二号板的连接处和纸箱输送辊道侧壁铰链,一号板一端和一推板气缸铰链,推板气缸铰链在纸箱输送辊道上。Further, the No. 1 baffle, the No. 2 baffle, and the No. 3 baffle are arranged on the carton conveying roller, and the No. 1 baffle, the No. 2 baffle and the No. 3 baffle are from the input end of the carton conveying roller to the The directions of the output ends are arranged in sequence. The No. 1 baffle and No. 3 baffle are pushed by the No. 1 baffle cylinder. The telescopic direction of the No. 1 baffle cylinder is perpendicular to the conveying direction of the carton conveying roller, and the No. 2 baffle includes the No. 1 baffle. There is an angle between the first plate and the second plate, the connection between the first plate and the second plate and the side wall hinge of the carton conveying roller, one end of the first plate and the cylinder hinge of the push plate, push The plate cylinder hinges on the carton conveying roller table.
进一步地,所述二号挡板、三号挡板之间设有导向组件,所述导向组件包括框型支架,框型支架通过竖直支架固定在纸箱输送辊道上方,框型支架内侧设有倾斜向下的柔性导向叶片,竖直支架上设有供框型支架滑动的滑条,纸箱输送辊道上设有推动框型支架上下移动的推动气缸。导向组件起导向作用,便于装箱。Further, a guide assembly is provided between the No. 2 baffle and the No. 3 baffle, and the guide assembly includes a frame-shaped bracket. The frame-shaped bracket is fixed above the carton conveying roller through a vertical bracket, and the inner side of the frame-shaped bracket is provided There are flexible guide vanes inclined downward, the vertical support is provided with a sliding bar for the frame-shaped support to slide, and the carton conveying roller is provided with a pushing cylinder for pushing the frame-shaped support to move up and down. The guide assembly plays a guiding role, which is convenient for packing.
进一步地,所述抓杆为圆柱状。Further, the grab bar is cylindrical.
进一步地,所述扇形齿条滑动杆上设有滚轮,扇形通孔和扇形齿条滑动杆通过滚轮滑动。扇形齿条及扇形齿条滑动杆不易损坏,运行平稳,噪音小。Further, a roller is provided on the sector-shaped rack sliding rod, and the fan-shaped through hole and the sector-shaped rack sliding rod slide through the roller. The fan-shaped rack and the sliding rod of the fan-shaped rack are not easy to be damaged, the operation is stable, and the noise is small.
本发明的有益效果是 :The beneficial effects of the present invention are:
1、本发明中的全自动装箱机工作效率高、定位准确、运行平稳、噪音小、不会损坏纸箱和液袋、易调节、方便后期维护。1. The fully automatic case packing machine in the present invention has high working efficiency, accurate positioning, stable operation, low noise, no damage to cartons and liquid bags, easy adjustment, and convenient later maintenance.
附图说明Description of drawings
图1为本发明的结构示意图。FIG. 1 is a schematic structural diagram of the present invention.
图2为纸箱输送辊道的结构示意图。Figure 2 is a schematic diagram of the structure of the carton conveying roller table.
图3为抓手的结构示意图。FIG. 3 is a schematic diagram of the structure of the gripper.
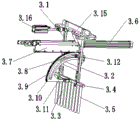
图4为抓手组件的结构示意图。FIG. 4 is a schematic structural diagram of the gripper assembly.
具体实施方式Detailed ways
下面将结合附图对本发明实施例中的技术方案进行清楚、完整地描述。The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the accompanying drawings.
实施例1:如图1、2、3、4所示,一种全自动装箱机,包括机架1、液袋输送辊道2、液袋抓手3、纸箱输送辊道4,纸箱输送辊道4和液袋输送辊道2垂直且存在间距,液袋抓手3位于纸箱输送辊道4和液袋输送辊道2之间并位于液袋输送辊道2的输出端端部;液袋抓手3包括两平行布置的抓手组件3.1,抓手组件3.1包括竖直布置的支架3.2、抓手3.3,抓手3.3包括一横杆3.4和若干并列布置在横杆3.4上的抓杆3.5,抓杆3.5为圆柱状;抓手3.3的横杆3.4与支架3.2铰链,支架3.2上还设有水平布置的抓手气缸3.6,抓手气缸3.6的活塞杆端部连接一直齿条3.7;支架3.2上设有一水平布置的扇形齿条滑动杆3.8,扇形齿条滑动杆3.8上设有一和直齿条3.7齿合的扇形齿条3.9,扇形齿条3.9上设有扇形通孔3.10,扇形齿条滑动杆3.8穿过扇形通孔3.10并和扇形齿条3.9板面方向垂直,扇形齿条滑动杆3.8上设有滚轮3.12,扇形通孔3.10和扇形齿条滑动杆3.8通过滚轮3.12滑动。扇形齿条3.9通过连接杆3.11和横杆3.4连接,连接杆3.11为扇形齿条3.9的半径;抓杆3.5位于水平状态时,两抓手组件3.1的抓杆3.5交错排列。两抓手组件3.1上方设有水平直线滑轨3.13,水平直线滑轨3.13中部设有支撑板3.14将水平直线滑轨3.13分隔为两段,两段上均设有滑块3.15,两抓手组件3.1分别设置在两滑块3.15上,抓手组件3.1的支架3.2顶部和滑块3.15底部连接,支撑板3.14上设有两水平布置的滑块气缸3.16分别和两滑块3.15连接。液袋抓手3通过移动组件5和机架1相连,移动组件5包括竖向移动机构6和水平移动机构7,水平直线滑轨3.13两端连接在竖向移动机构6上,竖向移动机构6连接在水平移动机构7上,水平移动机构7位于纸箱输送辊道4及纸箱输送辊道4和液袋输送辊道2的间距上方,水平移动机构7的移动方向和液袋输送辊道2的输送方向一致。水平移动机构7包括两平行布置的水平环形链条组7.1以及驱动水平环形链条组上的水平环形链条转动的驱动电机;竖向移动机构6包括位于水平环形链条上的竖直布置的竖直侧板6.1,竖直侧板6.1上设有竖直滑轨6.2及竖直环形链条组6.3以及驱动竖直环形链条组6.3的竖直环形链条转动的驱动电机,竖直滑轨6.2上设有在竖直滑轨6.2上滑动的竖直滑板6.4,竖直滑板6.4背面和竖直环形链条组6.3的竖直环形链条相连,抓手3的水平直线滑轨3.13的两端分别和两竖直侧板6.1上的竖直滑板6.4连接。纸箱输送辊道4上设有一号挡板4.1、二号挡板4.2、三号挡板4.3,一号挡板4.1、二号挡板4.2、三号挡板4.3从纸箱输送辊道4的输入端至输出端方向依次布置,所述一号挡板4.1、三号挡板4.3均通过一号挡板气缸4.4推动,一号挡板气缸4.4的伸缩方向和纸箱输送辊道4输送方向垂直,二号挡板4.2包括一号板4.21和二号板4.22,一号板4.21和二号板4.22之间存在夹角,一号板4.21和二号板4.22的连接处和纸箱输送辊道4侧壁铰链,一号板4.21一端和一推板气缸4.5铰链,推板气缸4.5铰链在纸箱输送辊道上。二号挡板4.2、三号挡板4.3之间设有导向组件8,导向组件8包括框型支架8.1,框型支架8.1通过竖直支架8.2固定在纸箱输送辊道4上方,框型支架8.1内侧设有倾斜向下的柔性导向叶片8.3,竖直支架8.2上设有供框型支架8.1滑动的滑条,纸箱输送辊道4上设有推动框型支架8.1上下移动的推动气缸8.4。Example 1: As shown in Figures 1, 2, 3, and 4, a fully automatic cartoning machine includes a
工作时,纸箱在纸箱输送辊道4上,由输入端至输出端运动,当纸箱完全经过一号挡板4.1后,一号挡板4.1伸出,使得后续的纸箱不会进入工作区域,然后三号挡板4.3伸出,使得纸箱停留在工作区域,无法继续前进,同时,二号挡板4.2伸出与三号挡板4.3配合,一前一后将纸箱固定住,这时,推动气缸8.4回退,带动其上的柔性导向叶片8.3进入箱口,在其后的装箱工程中起导向作用,便于装箱;液袋在液袋输送辊道2的带动下,最终落到液袋抓手3的抓杆3.5上,然后在竖直环形链条组6.3的带动下,液袋抓手3整体向上运动,使得液袋抓手3完全高于纸箱后,在水平环形链条组7.1的驱动下,运动到纸箱的上方,然后抓手气缸3.6伸出,直齿条3.7带着扇形齿条3.9转动,扇形齿条3.9带动抓手3.3转动,抓手3.3竖直,将液袋沿着柔性导向叶片8.3放入纸箱中。装箱动作结束,竖直环形链条组6.3带动抓手装置向上运动,然后再在水平环形链条组7.1下移动到液袋输送辊道2输出端的上方,然后再在竖直环形链条组6.3的带动下移,下移的同时抓手气缸3.6缩回,直齿条3.7带着扇形齿条3.9转动,扇形齿条3.9带动抓手3.3转动,抓手3.3水平,准备去抓取取下一个液袋。同时,推动气缸8.4顶出,使柔性导向叶片8.3不会干扰到纸箱的运行。二号挡板4.2、三号挡板4.3回退,使得纸箱顺利离开工作区域,当纸箱完全离开工作区域后,三号挡板4.3顶出,二号挡板4.2保持退回状态,一号挡板4.1回退,下一个纸箱开始进入工作区域,自动装箱机开始循环工作。When working, the carton moves from the input end to the output end on the
所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本发明保护的范围。The described embodiments are only some, but not all, embodiments of the present invention. Based on the embodiments of the present invention, all other embodiments obtained by those of ordinary skill in the art without creative efforts shall fall within the protection scope of the present invention.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010380929.7A CN111572881B (en) | 2020-05-08 | 2020-05-08 | Full-automatic case packer |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010380929.7A CN111572881B (en) | 2020-05-08 | 2020-05-08 | Full-automatic case packer |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN111572881A true CN111572881A (en) | 2020-08-25 |
| CN111572881B CN111572881B (en) | 2024-08-13 |
Family
ID=72113342
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010380929.7A Active CN111572881B (en) | 2020-05-08 | 2020-05-08 | Full-automatic case packer |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111572881B (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112046811A (en) * | 2020-09-11 | 2020-12-08 | 蚌埠天成包装科技股份有限公司 | Automatic box filling machine for liquid packaging film |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2016184006A1 (en) * | 2015-05-15 | 2016-11-24 | Tcl王牌电器(惠州)有限公司 | Carton flap-folding machine |
| CN206552333U (en) * | 2017-03-14 | 2017-10-13 | 湖南科伦制药有限公司 | One kind transfusion bag boxing machine |
| CN207774232U (en) * | 2018-01-15 | 2018-08-28 | 辽宁民康制药有限公司 | A kind of polypropylene infusion bag fast bottle cleaning device |
| CN212354570U (en) * | 2020-05-08 | 2021-01-15 | 无锡米多智能技术有限公司 | Full-automatic case packer |
-
2020
- 2020-05-08 CN CN202010380929.7A patent/CN111572881B/en active Active
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2016184006A1 (en) * | 2015-05-15 | 2016-11-24 | Tcl王牌电器(惠州)有限公司 | Carton flap-folding machine |
| CN206552333U (en) * | 2017-03-14 | 2017-10-13 | 湖南科伦制药有限公司 | One kind transfusion bag boxing machine |
| CN207774232U (en) * | 2018-01-15 | 2018-08-28 | 辽宁民康制药有限公司 | A kind of polypropylene infusion bag fast bottle cleaning device |
| CN212354570U (en) * | 2020-05-08 | 2021-01-15 | 无锡米多智能技术有限公司 | Full-automatic case packer |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112046811A (en) * | 2020-09-11 | 2020-12-08 | 蚌埠天成包装科技股份有限公司 | Automatic box filling machine for liquid packaging film |
Also Published As
| Publication number | Publication date |
|---|---|
| CN111572881B (en) | 2024-08-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN101792035B (en) | Automatic case unpacking machine | |
| CN111153220B (en) | A stacking mechanism for packing boxes | |
| CN111153224B (en) | An automatic stacking device for packaging boxes | |
| CN204751521U (en) | Pile up neatly forming device of material in hacking machine | |
| CN111572881B (en) | Full-automatic case packer | |
| CN209834115U (en) | A light bulb automatic packing machine | |
| CN212354570U (en) | Full-automatic case packer | |
| CN111619884B (en) | A packing device | |
| CN221498530U (en) | A side-push packaging box packing machine | |
| CN108974518B (en) | Automatic unpacking flip equipment | |
| CN206599025U (en) | A kind of empty van conveying mechanism for fall-off type casing device | |
| CN221163605U (en) | Packaging bag supporting device with underground driving follow-up supporting plate | |
| CN105460629A (en) | Folded plate disassembling mechanism for stacking machine | |
| CN202358338U (en) | Circular scraping packing type packing device | |
| CN211108400U (en) | Temporary storage device of cigarette case packaging production line | |
| CN115818327A (en) | Automatic integrated paper pushing equipment | |
| CN111619885A (en) | A collection device and packing production line | |
| CN204979370U (en) | Packing tube auto -incasing equipment | |
| CN223238127U (en) | A filling bottle conveying device | |
| CN223291874U (en) | An automatic depalletizer | |
| CN222137136U (en) | A lifting and pushing type automatic packing device | |
| CN223408717U (en) | A positioning and conveying mechanism for carton packaging printing | |
| CN213384913U (en) | Large-size boxing machine | |
| CN204415775U (en) | A kind of case packer packing multi-brand barrel | |
| CN222769659U (en) | Automatic book picking and placing device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| PE01 | Entry into force of the registration of the contract for pledge of patent right |
Denomination of invention: A fully automatic packing machine Granted publication date: 20240813 Pledgee: Bank of China Limited Yixing branch Pledgor: Wuxi Mido Intelligent Technology Co.,Ltd. Registration number: Y2024980049665 |
|
| PE01 | Entry into force of the registration of the contract for pledge of patent right |