CN111420842B - Automatic lubricant dip-coating equipment for automobile wheel balance block - Google Patents
Automatic lubricant dip-coating equipment for automobile wheel balance block Download PDFInfo
- Publication number
- CN111420842B CN111420842B CN202010329541.4A CN202010329541A CN111420842B CN 111420842 B CN111420842 B CN 111420842B CN 202010329541 A CN202010329541 A CN 202010329541A CN 111420842 B CN111420842 B CN 111420842B
- Authority
- CN
- China
- Prior art keywords
- blank
- blanking
- transition
- transfer
- supporting plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 239000000314 lubricant Substances 0.000 title claims abstract description 98
- 238000003618 dip coating Methods 0.000 title claims abstract description 93
- 230000007246 mechanism Effects 0.000 claims abstract description 128
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims abstract description 60
- 229910002804 graphite Inorganic materials 0.000 claims abstract description 60
- 239000010439 graphite Substances 0.000 claims abstract description 60
- 238000000034 method Methods 0.000 claims abstract description 44
- 230000008569 process Effects 0.000 claims abstract description 40
- 239000007788 liquid Substances 0.000 claims abstract description 31
- 238000004064 recycling Methods 0.000 claims abstract description 28
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 15
- 239000011248 coating agent Substances 0.000 claims abstract description 11
- 238000000576 coating method Methods 0.000 claims abstract description 11
- 238000001125 extrusion Methods 0.000 claims abstract description 9
- 230000007704 transition Effects 0.000 claims description 120
- 230000005540 biological transmission Effects 0.000 claims description 54
- 238000011084 recovery Methods 0.000 claims description 25
- 230000003139 buffering effect Effects 0.000 claims description 17
- 239000000463 material Substances 0.000 claims description 17
- 238000003756 stirring Methods 0.000 claims description 12
- 238000007598 dipping method Methods 0.000 claims description 7
- 238000010992 reflux Methods 0.000 claims description 4
- 238000005086 pumping Methods 0.000 claims description 2
- 230000007423 decrease Effects 0.000 claims 1
- 238000002791 soaking Methods 0.000 abstract description 4
- 238000002360 preparation method Methods 0.000 abstract description 3
- 230000001050 lubricating effect Effects 0.000 abstract 1
- 239000003974 emollient agent Substances 0.000 description 15
- 230000033001 locomotion Effects 0.000 description 11
- 238000004512 die casting Methods 0.000 description 4
- 238000011068 loading method Methods 0.000 description 4
- 239000002184 metal Substances 0.000 description 3
- 229910052751 metal Inorganic materials 0.000 description 3
- CWYNVVGOOAEACU-UHFFFAOYSA-N Fe2+ Chemical compound [Fe+2] CWYNVVGOOAEACU-UHFFFAOYSA-N 0.000 description 2
- 238000013459 approach Methods 0.000 description 2
- 125000004122 cyclic group Chemical group 0.000 description 2
- 238000001514 detection method Methods 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 230000032258 transport Effects 0.000 description 2
- 229910000978 Pb alloy Inorganic materials 0.000 description 1
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 1
- 229910001297 Zn alloy Inorganic materials 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000010790 dilution Methods 0.000 description 1
- 239000012895 dilution Substances 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 238000001035 drying Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000000605 extraction Methods 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000011701 zinc Substances 0.000 description 1
Images







Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C3/00—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material
- B05C3/02—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material the work being immersed in the liquid or other fluent material
- B05C3/09—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material the work being immersed in the liquid or other fluent material for treating separate articles
- B05C3/10—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material the work being immersed in the liquid or other fluent material for treating separate articles the articles being moved through the liquid or other fluent material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C11/00—Component parts, details or accessories not specifically provided for in groups B05C1/00 - B05C9/00
- B05C11/10—Storage, supply or control of liquid or other fluent material; Recovery of excess liquid or other fluent material
- B05C11/1039—Recovery of excess liquid or other fluent material; Controlling means therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C13/00—Means for manipulating or holding work, e.g. for separate articles
- B05C13/02—Means for manipulating or holding work, e.g. for separate articles for particular articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C9/00—Apparatus or plant for applying liquid or other fluent material to surfaces by means not covered by any preceding group, or in which the means of applying the liquid or other fluent material is not important
- B05C9/08—Apparatus or plant for applying liquid or other fluent material to surfaces by means not covered by any preceding group, or in which the means of applying the liquid or other fluent material is not important for applying liquid or other fluent material and performing an auxiliary operation
- B05C9/12—Apparatus or plant for applying liquid or other fluent material to surfaces by means not covered by any preceding group, or in which the means of applying the liquid or other fluent material is not important for applying liquid or other fluent material and performing an auxiliary operation the auxiliary operation being performed after the application
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16N—LUBRICATING
- F16N15/00—Lubrication with substances other than oil or grease; Lubrication characterised by the use of particular lubricants in particular apparatus or conditions
- F16N15/02—Lubrication with substances other than oil or grease; Lubrication characterised by the use of particular lubricants in particular apparatus or conditions with graphite or graphite-containing compositions
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16N—LUBRICATING
- F16N15/00—Lubrication with substances other than oil or grease; Lubrication characterised by the use of particular lubricants in particular apparatus or conditions
- F16N15/04—Lubrication with substances other than oil or grease; Lubrication characterised by the use of particular lubricants in particular apparatus or conditions with water
Landscapes
- Engineering & Computer Science (AREA)
- General Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Coating Apparatus (AREA)
Abstract
The invention relates to the field of automobile part processing, in particular to an automatic lubricant dip-coating device for an automobile wheel balance block, which comprises a blank dip-coating mechanism, a blank draining mechanism, a lubricant recycling mechanism, a stacking blanking mechanism and a lubricating mechanism, wherein the blank dip-coating mechanism is used for soaking a preheated blank to perform a subsequent extrusion process, the blank draining mechanism is arranged at the side part of the blank dip-coating mechanism and is used for draining off the water aqua graphite lubricant left on the blank in the blank transferring process, the lubricant recycling mechanism is arranged at the bottom part of the blank draining mechanism and is used for recycling the water aqua graphite lubricant drained by the blank draining mechanism and returning the water aqua graphite lubricant into the blank dip-coating mechanism to perform the recycling of the water aqua graphite lubricant, the stacking blanking mechanism is arranged at the side part of the blank draining mechanism and is used for completing the blanking process of the blank after residual liquid is drained, the automatic lubricant coating and residual liquid draining processes on the blank of the automobile wheel balance block are met, in preparation for the subsequent extrusion process.
Description
Technical Field
The invention relates to the field of automobile part processing, in particular to an automatic lubricant dip-coating device for an automobile wheel balance block.
Background
In the manufacturing process of the automobile wheel, due to factors such as processing technology and materials, absolute concentricity cannot be guaranteed between a shaft and a hub, and a certain eccentric distance exists. When the automobile keeps running at a high speed, the automobile can generate violent jolt, and the performance and the safety of the automobile are influenced. Therefore, before the wheels are installed, the dynamic balance check must be carried out, and one to a plurality of balance weights with different weights need to be installed on each wheel according to the check result of the dynamic balance. Currently, automobile wheel balance weights are basically formed by non-ferrous metal die-casting, such as zinc or lead alloy. Embedding the spring hanger into the die cavity before die-casting, wrapping the spring hanger by the formed metal after die-casting, and clamping the spring hanger on the balance block on the hub of the automobile wheel. The automobile wheel balance block formed by non-ferrous metal die-casting has the characteristics of good forming performance, simpler forming process and the like.
The application proposes to provide an automatic dip-coating lubricant device for the automobile wheel balance block meeting the manufacturing process, and meets the procedures of automatically coating the lubricant and draining residual liquid for the automobile wheel balance block blank so as to prepare for carrying out subsequent extrusion procedures.
Disclosure of Invention
The technical scheme meets the procedures of automatically coating the lubricant and draining residual liquid for the automobile wheel balance block blank so as to prepare for the subsequent extrusion procedure.
In order to solve the technical problems, the invention provides the following technical scheme:
provides an automatic lubricant dip-coating device for a vehicle wheel balance block, which comprises
The blank dip-coating mechanism is filled with aqueous graphite lubricant diluted according to the ratio of 1: 1, and the aqueous graphite lubricant is used for soaking the preheated blank to perform the subsequent extrusion process;
the blank draining mechanism is arranged on the side part of the blank dip-coating mechanism, and the input end of the blank draining mechanism is connected with the output end of the blank dip-coating mechanism and is used for transferring the soaked blank and draining the residual aqueous graphite lubricant on the blank in the blank transferring process;
the lubricant recovery mechanism is arranged at the bottom of the blank draining mechanism and used for recovering the water aqua graphite lubricant drained and thrown off by the blank draining mechanism and refluxing the water aqua graphite lubricant into the blank dip-coating mechanism for recycling the water aqua graphite lubricant;
and the stacking and blanking mechanism is arranged on the side part of the blank draining mechanism, and the input end of the stacking and blanking mechanism is connected with the output end of the blank draining mechanism, so that the blanking process of the blank after residual liquid is drained can be completed, and the blank can be automatically stacked.
As a preferred scheme of the automatic lubricant dip-coating equipment for the automobile wheel balance block, the blank dip-coating mechanism comprises a dip-coating box, a feeding pipeline, a transfer driving motor, a transfer gear set, a feeding guide plate and a buffer rail, dip-coating incasement splendid attire according to the dilution aqueous graphite emollient, the both ends of dip-coating case are equipped with respectively the feeding pipeline with buffering track, the lateral wall of dip-coating case is equipped with shift driving motor shifts driving motor transmission and is connected with the setting in the dip-coating incasement shift gear group shifts the gear train, shifts the gear train from the direction of feeding pipeline to the material deflector tilt up gradually and sets up, and the one end that the shift gear train is close to the material loading deflector exceeds the liquid level of aqueous graphite emollient, and the top of shift gear train is equipped with a pair ofly the material loading deflector, interval between two material loading deflectors diminishes gradually from the direction of feeding pipeline to the material loading deflector.
As an optimal scheme of the automatic lubricant dip-coating equipment for the automobile wheel balance block, a stirring driving motor is arranged at the bottom of a dip-coating box, and an output shaft of the stirring driving motor penetrates through the dip-coating box and is in transmission connection with a stirring shaft.
As an automatic dip-coating lubricant equipment's of auto wheel balancing piece preferred scheme, the buffering track includes first backup pad, first buffering roller, second backup pad and second buffering roller, first backup pad with the second backup pad is fixed on the lateral wall of dip-coating case, first backup pad and second backup pad parallel arrangement, and first backup pad is good at the second backup pad setting, rotates between first backup pad and the second backup pad and is connected with a plurality of intervals and equals first buffering roller, first buffering roller are close to dip-coating case setting, and the part that the second backup pad was good at to first backup pad rotates and is connected with a plurality of intervals and equals second buffering roller, interval between the second buffering roller are greater than interval between the first buffering roller.
As a preferred scheme of the automatic lubricant dip-coating equipment for the automobile wheel balance block, the blank draining mechanism comprises a first lifting support, a first driving motor, a first belt transmission module, a first transfer table, a second lifting support, a second driving motor, a second belt transmission module, a second transfer table, a transition driving motor, a blanking table and a blanking guide roller, wherein the first lifting support is arranged at the side part of the buffering track, the first lifting support is provided with the first driving motor, the first driving motor is in transmission connection with the first belt transmission module, the side part of the first belt transmission module is provided with the first transfer table, the first transfer table is in sliding connection with the first lifting support and slides along the height direction of the first lifting support, the first transfer table is matched with the buffering track, the input end of the first transfer table is connected with the output end of the buffering track, the second lifting support is arranged on the side part of the first lifting support, the second driving motor is arranged on the second lifting support, the second driving motor is in transmission connection with the second belt transmission module, the second transfer table is arranged on the side part of the second belt transmission module, the second transfer table is in sliding connection with the second lifting support and slides along the height direction of the second lifting support, the transition table is arranged between the first lifting support and the second lifting support, the transition table is arranged at the top end of the first lifting support and the top end of the second lifting support, the transition driving motor is arranged at the top of the transition table, the output end of the transition driving motor is in transmission connection with the transition table, the transition table is matched with the first transfer table, the input end of the transition table is connected with the output end of the first transfer table, the second transfer table is matched with the transition table, and the input end of the second transfer table is connected with the output end of the transition table, the bottom of second lifting support is equipped with the unloading platform, the unloading platform cooperatees with second transfer table, and the input of unloading platform is connected with the output of second transfer table, and the output of unloading platform is equipped with a pair ofly the unloading guide roll, the interval between two unloading guide rolls diminishes from the input of unloading platform to the output of unloading platform gradually.
As a preferred scheme of the automatic lubricant dip-coating equipment for the automobile wheel balance block, the transition table comprises a third support plate, a transition transmission belt module, a first transition roller, a fourth support plate, a second transition roller and a third transition roller, wherein the third support plate and the fourth support plate are positioned at the top ends of a first lifting support and a second lifting support, the third support plate and the fourth support plate are arranged in parallel, two ends of the third support plate extend out of the fourth support plate, a plurality of first transition rollers with equal intervals are rotatably connected between the third support plate and the fourth support plate, one end of the third support plate close to the first lifting support is rotatably connected with a plurality of second transition rollers with equal intervals, one end of the third support plate close to the second lifting support is rotatably connected with a plurality of third transition rollers with equal intervals, and the intervals between the second transition rollers are larger than the intervals between the first transition rollers, the interval is greater than the interval between the first transition roller between the third transition roller, is equipped with in the third backup pad transition driving belt module, transition driving motor's output and transition driving belt module transmission are connected, and transition driving belt module drives first transition roller, second transition roller and third transition roller and rotates.
As a preferred scheme of the automatic lubricant dipping and coating equipment for the automobile wheel balance block, the blanking table comprises a fifth supporting plate, a blanking transmission belt module, a first blanking roller, a sixth supporting plate, a second blanking roller, a supporting underframe and a deviation-rectifying driving cylinder, wherein the fifth supporting plate and the sixth supporting plate are positioned on one side of a second lifting support far away from the first lifting support, the fifth supporting plate and the sixth supporting plate are arranged in parallel, one end of the fifth supporting plate close to the second lifting support extends out of the sixth supporting plate, a plurality of first blanking rollers with equal intervals are rotatably connected between the fifth supporting plate and the sixth supporting plate, one end of the fifth supporting plate extending out of the sixth supporting plate is rotatably connected with a plurality of second blanking rollers with equal intervals, the intervals between the second blanking rollers are larger than the intervals between the first blanking rollers, and the blanking transmission belt module for driving the first blanking roller and the second blanking roller to rotate is arranged on the fifth supporting plate, the bottom of the first blanking roller is provided with the supporting bottom frame, the supporting bottom frame is provided with the deviation rectifying driving cylinder, the output end of the deviation rectifying driving cylinder is provided with a pair of first deviation rectifying columns and a pair of second deviation rectifying columns, a certain gap exists between the two first deviation rectifying columns and penetrates through one of the first blanking rollers, the second deviation rectifying columns are located on the side portions of the first deviation rectifying columns, and a certain gap exists between the two second deviation rectifying columns and penetrates through the first blanking rollers through which the two first deviation rectifying columns penetrate.
As a preferred scheme of the automatic lubricant dip-coating equipment for the automobile wheel balance block, a first transfer platform comprises a first frame, a first slide rail, a first slide block and a first transfer roller, the first frame slides along the height direction of a first lifting support, the first slide rail is arranged on the first frame, the first slide rail is connected with the first slide block in a sliding manner, one end face of the first slide block is rotatably connected with a plurality of first transfer rollers with equal intervals, a gap between adjacent second buffer rollers is used for the first transfer roller to pass through, a gap between adjacent second transition rollers is used for the first transfer roller to pass through, the second transfer platform comprises a second frame, a second slide rail, a second slide block and a second transfer roller, the second frame slides along the height direction of the first lifting support, the second slide rail is arranged on the second frame, and the second slide rail is connected with the second slide block in a sliding manner, one end face of the second sliding block is rotatably connected with a plurality of second transfer rollers with equal intervals, a gap between every two adjacent second discharging rollers is used for the second transfer rollers to pass through, and a gap between every two adjacent third transition rollers is used for the second transfer rollers to pass through.
As an automatic dip-coating lubricant equipment's of auto wheel balancing piece preferred scheme, emollient is retrieved the mechanism and is included return line, first pipeline, collection box, second pipeline and pump machine, the return line sets up in blank drip dry bottom of mechanism, and the one end intercommunication of return line has first pipeline, the other end intercommunication of first pipeline have the collection box is equipped with the drawing liquid pipeline on, the collection box, and collection box inside is equipped with first level sensor and second level sensor, first level sensor is located second level sensor top, is equipped with on dip-coating box's the lateral wall the pump machine, the pump machine passes through second pipeline and collection box intercommunication.
As a preferred scheme of the automatic lubricant dipping and coating equipment for the automobile wheel balance block, the stacking and blanking mechanism comprises a supporting table, a material pushing cylinder, a blank fixture, a first lead screw sliding table, a second lead screw sliding table, a pneumatic clamping jaw, a blanking sliding table and a stacking box, wherein the supporting table is arranged on one side, away from the second lifting support, of the blanking table, one end, close to the blanking table, of the supporting table is provided with the material pushing cylinder, the blank fixture is arranged beside the output end of the material pushing cylinder and comprises a fixed plate, a sliding protrusion and a sliding plate, the fixed plate is connected with the sliding plate in a sliding manner, the sliding plate is provided with the sliding protrusion with intervals, the supporting table is provided with the first lead screw sliding table, the first lead screw sliding table is positioned on the side part of the blank fixture, the first lead screw sliding table is connected with the second lead screw, the supporting table is provided with a feed opening, the bottom end of the feed opening is provided with the feed sliding table, and the output end of the feed sliding table is provided with the stacking box.
Compared with the prior art, the invention has the beneficial effects that:
firstly, the preheated blank is put into a blank dip-coating mechanism, and the blank is completely dipped in the aqueous graphite lubricant, the automatic dip-coating process of the aqueous graphite lubricant is completed in the blank dip-coating mechanism, then the blank dip-coating mechanism conveys the blank to the blank draining mechanism, after a series of conveying processes of the blank draining mechanism, the residual aqueous graphite lubricant on the blank is drained, the aqueous graphite lubricant falling from the blank falls into a lubricant recovery mechanism, and is recovered by the lubricant recovery mechanism, the lubricant recovery mechanism then returns the aqueous graphite lubricant to the blank dip-coating mechanism for recycling the aqueous graphite lubricant, when the blank draining mechanism conveys the blank to the output end of the blank draining mechanism, the stacking and blanking mechanism receives the blanks from the blank draining mechanism, performs the blanking process of the blanks and automatically stacks the blanks in the process.
This dip-coating emollient equipment satisfies automatic coating emollient and the driping raffinate process to auto wheel balancing piece blank, in order to carry out subsequent extrusion process, through having set up blank driping mechanism, go up and down at first transfer station, the transfer of transition platform, the transfer process of second transfer station lift and unloading platform, can fully driping remaining aqueous graphite emollient on the blank, in the emollient retrieves mechanism gets into aqueous graphite emollient backward flow blank dip-coating mechanism again, carry out aqueous graphite emollient's cyclic utilization, whole process degree of automation is high, make the auto wheel balancing piece performance of preparation better.
Drawings
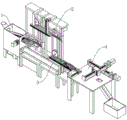
FIG. 1 is a schematic structural view of the present invention;
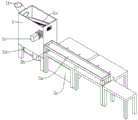
FIG. 2 is a schematic structural diagram of a blank dip coating mechanism according to the present invention;
FIG. 3 is a schematic view of the structure of the buffer rail of the present invention;
FIG. 4 is a schematic structural diagram of a blank dip-coating mechanism and a lubricant recovery mechanism according to the present invention;
FIG. 5 is a side view of the present invention at the billet dip coating mechanism and the lubricant reclaim mechanism;
FIG. 6 is a schematic cross-sectional view taken along line A-A of FIG. 5;
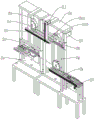
FIGS. 7 and 8 are schematic views of the billet drying mechanism of the present invention from two different perspectives;
FIG. 9 is a schematic view of the structure at the transition station of the present invention;
FIGS. 10 and 11 are schematic views of the blanking table of the present invention from two different viewing angles;
FIG. 12 is an enlarged view at A of FIG. 11;
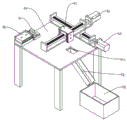
fig. 13 and 14 are schematic structural views of the stacking and blanking mechanism of the invention.
The reference numbers in the figures are:
1-a blank dip-coating mechanism; 1 a-dip coating tank; 1 b-a feed conduit; 1 c-a transfer drive motor; 1 d-transfer gear set; 1 e-a feeding guide plate; 1 f-buffer rail; 1f1 — first support plate; 1f2 — first buffer roller; 1f3 — second support plate; 1f4 — second buffer roller; 1 g-stirring driving motor; 1 h-stirring shaft;
2-a blank draining mechanism; 2 a-a first lifting bracket; 2 b-a first drive motor; 2 c-a first belt transmission module; 2 d-first transfer stage; 2d1 — first frame; 2d2 — first slide; 2d3 — first slider; 2d4 — first transfer roll; 2 e-a second lifting support; 2 f-a second drive motor; 2 g-a second belt transmission module; 2 h-a second transfer table; 2h1 — second frame; 2h2 — second slide; 2h3 — second slider; 2h4 — second transfer roll; 2 i-a transition table; 2i 1-third support plate; 2i 2-transition drive belt module; 2i3 — first transition roll; 2i 4-fourth support plate; 2i5 — second transition roll; 2i6 — third transition roll; 2 j-transition drive motor; 2 k-a blanking table; 2k 1-fifth support plate; 2k 2-a blanking transmission belt module; 2k3 — first down roll; 2k 4-sixth support plate; 2k5 — second feed roll; 2k6 — support chassis; 2k 7-deviation rectifying driving cylinder; 2k 8-first deviation rectifying column; 2k 9-second deviation rectifying column; 2 l-a blanking guide roller;
3-a lubricant recovery mechanism; 3 a-a recovery pipeline; 3 b-a first conduit; 3 c-a recovery tank; 3c1 — first level sensor; 3c2 — second liquid level sensor; 3c 3-liquid extraction pipe; 3 d-a second conduit; 3 e-a pump;
4-stacking and blanking mechanism; 4 a-a support table; 4a 1-feed opening; 4 b-a material pushing cylinder; 4 c-a blank fixture; 4c 1-dead plate; 4c 2-sliding projection; 4c 3-sliding plate; 4 d-a first screw rod sliding table; 4 e-a second screw rod sliding table; 4 f-pneumatic jaws; 4 g-a blanking sliding table; 4 h-stacking the boxes;
5-blank.
Detailed Description
In order to make the objects, technical solutions and advantages of the present invention more apparent, the present invention is described in further detail below with reference to the accompanying drawings and embodiments. It should be understood that the specific embodiments described herein are merely illustrative of the invention and are not intended to limit the invention.
In the description of the present invention, it should be noted that the terms "center", "upper", "lower", "left", "right", "front", "rear", "vertical", "horizontal", "inner", "outer", and the like indicate orientations or positional relationships based on those shown in the drawings, and are only for convenience of description and simplicity of description, but do not indicate or imply that the referred device or element must have a specific orientation, be constructed in a specific orientation, and be operated, and thus, should not be construed as limiting the present invention. Furthermore, the terms "first," "second," and "third" are used for descriptive purposes only and are not to be construed as indicating or implying relative importance.
Referring to FIG. 1, the apparatus for dip coating lubricant comprises
The blank dip-coating mechanism 1 is filled with aqueous graphite lubricant diluted by 1: 1, and the aqueous graphite lubricant is used for soaking the preheated blank 5 to carry out the subsequent extrusion process;
the blank draining mechanism 2 is arranged on the side part of the blank dip-coating mechanism 1, the input end of the blank draining mechanism 2 is connected with the output end of the blank dip-coating mechanism 1, and the blank draining mechanism is used for transferring the soaked blank 5 and draining the residual aqueous graphite lubricant on the blank 5 in the process of transferring the blank 5;
the lubricant recovery mechanism 3 is arranged at the bottom of the blank draining mechanism 2 and used for recovering the water aqua graphite lubricant drained and thrown off by the blank draining mechanism 2 and refluxing the water aqua graphite lubricant into the blank dip-coating mechanism 1 for recycling the water aqua graphite lubricant;
and the stacking and blanking mechanism 4 is arranged on the side part of the blank draining mechanism 2, and the input end of the stacking and blanking mechanism 4 is connected with the output end of the blank draining mechanism 2, so that the blanking process of the blank 5 after residual liquid is drained can be completed, and the blank is automatically stacked.
When the lubricant dip-coating equipment works, a preheated blank 5 is firstly placed into a blank dip-coating mechanism 1, the blank 5 is completely immersed in the aqueous graphite lubricant, the automatic dip-coating process of the aqueous graphite lubricant is completed in the blank dip-coating mechanism 1, then the blank dip-coating mechanism 1 conveys the blank 5 to a blank draining mechanism 2, after a series of conveying processes of the blank draining mechanism 2, the aqueous graphite lubricant remained on the blank 5 is drained, the aqueous graphite lubricant falling from the blank 5 falls into a lubricant recovery mechanism 3 and is recovered by the lubricant recovery mechanism 3, the lubricant recovery mechanism 3 returns the aqueous graphite lubricant to the blank dip-coating mechanism 1 for recycling the aqueous graphite lubricant, when the blank 5 is conveyed to the output end of the blank draining mechanism 2, a stacking and blanking mechanism 4 receives the blank 5 from the blank draining mechanism 2, the blanking process of the blank 5 is performed, and the blank 5 is automatically stacked in the process.
Referring to fig. 2, the blank dip-coating mechanism 1 includes a dip-coating tank 1a, a feeding pipe 1b, and a transfer driving motor 1c, the device comprises a transfer gear set 1d, feeding guide plates 1e and a buffer track 1f, wherein aqueous graphite lubricant diluted according to the ratio of 1: 1 is contained in a dip-coating box 1a, a feeding pipeline 1b and the buffer track 1f are respectively arranged at two ends of the dip-coating box 1a, a transfer driving motor 1c is arranged on the outer side wall of the dip-coating box 1a, the transfer driving motor 1c is in transmission connection with a transfer gear set 1d arranged in the dip-coating box 1a, the transfer gear set 1d is gradually and upwards inclined from the feeding pipeline 1b to the feeding guide plates 1e, one end, close to the feeding guide plates 1e, of the transfer gear set 1d is higher than the liquid level of the aqueous graphite lubricant, a pair of feeding guide plates 1e is arranged at the top of the transfer gear set 1d, and the distance between the two feeding guide plates 1e is gradually reduced from the feeding pipeline 1b to the feeding guide plates 1 e. The blank 5 is put into the dip-coating box 1a from the feeding pipeline 1b, when the transfer driving motor 1c works, the transfer gear set 1d is driven to rotate, when the transfer gear set 1d rotates, the blank 5 on the transfer gear set is conveyed to the buffer track 1f from the feeding pipeline 1b, and the blank 5 soaked in the aqueous graphite lubricant is lifted above the liquid level of the aqueous graphite lubricant, and in the process, the blank 5 finishes the dip-coating process of the lubricant.
Referring to fig. 6, a stirring driving motor 1g is arranged at the bottom of the dip-coating box 1a, an output shaft of the stirring driving motor 1g penetrates through the dip-coating box 1a and is in transmission connection with a stirring shaft 1h, when the stirring driving motor 1g works, the aqueous graphite lubricant in the dip-coating box 1a is stirred uniformly, and the dip-coating effect of the blank 5 immersed in the aqueous graphite lubricant is better.
Referring to fig. 3, the buffer rail 1f includes a first support plate 1f1, a first buffer roller 1f2, a second support plate 1f3 and a second buffer roller 1f4, the first support plate 1f1 and the second support plate 1f3 are fixed on the outer sidewall of the dip coating tank 1a, the first support plate 1f1 and the second support plate 1f3 are arranged in parallel, the first support plate 1f1 is longer than the second support plate 1f3, a plurality of first buffer rollers 1f2 with equal intervals are rotatably connected between the first support plate 1f1 and the second support plate 1f3, the first buffer roller 1f2 is arranged close to the dip coating tank 1a, a plurality of second buffer rollers 1f4 with equal intervals are rotatably connected to the portion of the first support plate 1f1 longer than the second support plate 1f3, and the interval between the second buffer rollers 1f4 is greater than the interval between the first buffer rollers 1f 2. When the transfer gear set 1d transports the blank 5 onto the buffer rail 1f, the blank 5 will slide a distance on the first buffer roller 1f2 and onto the second buffer roller 1f4 due to the inertia of the movement of the blank 5.
Referring to fig. 7 and 8, the blank draining mechanism 2 includes a first lifting bracket 2a, a first driving motor 2b, a first belt transmission module 2c, a first transfer table 2d, a second lifting bracket 2e, a second driving motor 2f, a second belt transmission module 2g, a second transfer table 2h, a transition table 2i, a transition driving motor 2j, a blanking table 2k and a blanking guide roller 2l, the first lifting bracket 2a is disposed at a side portion of the buffer rail 1f, the first lifting bracket 2a is provided with a first driving motor 2b, the first driving motor 2b is in transmission connection with the first belt transmission module 2c, the side portion of the first belt transmission module 2c is provided with a first transfer table 2d, the first transfer table 2d is in sliding connection with the first lifting bracket 2a, slides along a height direction of the first lifting bracket 2a, the first transfer table 2d is matched with the buffer rail 1f, the input end of a first transfer platform 2d is connected with the output end of a buffer track 1f, the side part of the first lifting support 2a is provided with a second lifting support 2e, the second lifting support 2e is provided with a second driving motor 2f, the second driving motor 2f is connected with a second belt transmission module 2g in a transmission way, the side part of the second belt transmission module 2g is provided with a second transfer platform 2h, the second transfer platform 2h is connected with the second lifting support 2e in a sliding way and slides along the height direction of the second lifting support 2e, a transition platform 2i is arranged between the first lifting support 2a and the second lifting support 2e, the transition platform 2i is arranged at the top end of the first lifting support 2a and the second lifting support 2e, the top part of the transition platform 2i is provided with a transition driving motor 2j, the output end of the transition driving motor 2j is connected with the transition platform 2i in a transmission way, the transition platform 2i is matched with the first transfer platform 2d, the input of transition platform 2i is connected with first transfer table 2 d's output, second transfer table 2h cooperatees with transition platform 2i, second transfer table 2 h's input is connected with transition platform 2 i's output, second lifting support 2 e's bottom is equipped with unloading platform 2k, unloading platform 2k cooperatees with second transfer table 2h, unloading platform 2 k's input is connected with second transfer table 2 h's output, unloading platform 2 k's output is equipped with a pair of unloading guide roll 2l, interval between two unloading guide roll 2l diminishes from unloading platform 2 k's input to unloading platform 2 k's output gradually. When the first driving motor 2b works, the first belt transmission module 2c is driven to work, when the first belt transmission module 2c works, the first transfer table 2d is driven to carry out lifting motion along the height direction of the first lifting support 2a, similarly, when the second driving motor 2f works, the second belt transmission module 2g works, when the second belt transmission module 2g works, the second transfer table 2h is driven to carry out lifting motion along the height direction of the second lifting support 2e, when the first transfer table 2d carries out lifting motion, the blank 5 is carried by the approaching buffer track 1f, and the blank 5 is transferred to the transition table 2i, when the second transfer table 2h carries out lifting motion, the blank 5 is carried by the approaching transition table 2i, and the blank 5 is transferred to the blanking table 2k, when the transition table 2i works, the blank 5 transferred from the first transfer table 2d is received, the blank 5 is transferred from one end of the transition table 2i to the other end of the transition table 2i for the second transfer table 2h to carry, and the blanking table 2k receives the blank 5 transferred from the second transfer table 2h during working, and transfers the blank 5 to the stacking and blanking mechanism 4.
Referring to fig. 9, the transition table 2i includes a third support plate 2i1, a transition transmission belt module 2i2, a first transition roller 2i3, a fourth support plate 2i4, a second transition roller 2i5 and a third transition roller 2i6, the third support plate 2i1 and the fourth support plate 2i4 are located at the top ends of the first lifting bracket 2a and the second lifting bracket 2e, the third support plate 2i1 and the fourth support plate 2i4 are arranged in parallel, two ends of the third support plate 2i1 extend out of the fourth support plate 2i4, a plurality of first transition rollers 2i3 with equal intervals are rotatably connected between the third support plate 2i1 and the fourth support plate 2i4, a plurality of second transition rollers 2i5 with equal intervals are rotatably connected at an end of the third support plate 2i1 close to the first lifting bracket 2a, a plurality of third transition rollers 6 with equal intervals are rotatably connected at an end of the third support plate 2i1 close to the second lifting bracket 2e, the interval between the second transition roller 2i5 is greater than the interval between the first transition roller 2i3, the interval is greater than the interval between the first transition roller 2i3 between the third transition roller 2i6, be equipped with transition driving belt module 2i2 on the third backup pad 2i1, the output of transition driving motor 2j is connected with the transmission of transition driving belt module 2i2 transmission, transition driving belt module 2i2 drives first transition roller 2i3, second transition roller 2i5 and third transition roller 2i6 and rotates.
Referring to fig. 10, 11 and 12, the blanking table 2k includes a fifth support plate 2k1, a blanking transmission belt module 2k2, a first blanking roller 2k3, a sixth support plate 2k4, a second blanking roller 2k5, a support chassis 2k6 and a deviation-correcting driving cylinder 2k7, the fifth support plate 2k1 and the sixth support plate 2k4 are located at one side of the second lifting bracket 2e away from the first lifting bracket 2a, the fifth support plate 2k1 and the sixth support plate 2k4 are arranged in parallel, one end of the fifth support plate 2k1 close to the second lifting bracket 2e extends out of the sixth support plate 2k4, a plurality of first blanking rollers 2k3 with equal intervals are rotatably connected between the fifth support plate 2k1 and the sixth support plate 2k4, one end of the fifth support plate 2k1 extending out of the sixth support plate 2k4 is rotatably connected with a plurality of second blanking rollers 2k5 with equal intervals, and the second blanking rollers 5 k3 k are larger than the intervals between the second blanking rollers 3 k 362 k3 k, the fifth supporting plate 2k1 is provided with a blanking transmission belt module 2k2 for driving the first blanking roller 2k3 and the second blanking roller 2k5 to rotate, the bottom of the first blanking roller 2k3 is provided with a supporting bottom frame 2k6, the supporting bottom frame 2k6 is provided with a deviation-rectifying driving cylinder 2k7, the output end of the deviation-rectifying driving cylinder 2k7 is provided with a pair of first deviation-rectifying columns 2k8 and a pair of second deviation-rectifying columns 2k9, a certain gap exists between the two first deviation-rectifying columns 2k8 and penetrates through one first blanking roller 2k3, the second deviation-rectifying columns 2k9 are located at the side parts of the first deviation-rectifying columns 2k8, a certain gap exists between the two second deviation-rectifying columns 2k9 and penetrates through the first blanking rollers 2k3 through which the two first deviation-rectifying columns 2k8 penetrate. The blanking guide roller 2l has a similar function to the feeding guide plate 1e and is used for guiding the blank 5, so that the blank 5 can smoothly reach the stacking blanking mechanism 4 or the buffer rail 1f, when the deviation-rectifying driving cylinder 2k7 works, the gap between the first deviation-rectifying column 2k8 and the second deviation-rectifying column 2k9 is used for the blank 5 to pass through, therefore, the positions of the first deviation-rectifying column 2k8 and the second deviation-rectifying column 2k9 can be changed by the deviation-rectifying driving cylinder 2k7, the movement track of the blank 5 is rectified, and the blank 5 is ensured to smoothly enter the blanking guide roller 2l and enter the stacking blanking mechanism 4 along a line specified by the blanking guide roller 2 l.
Referring to fig. 3, the first relay station 2d includes a first frame 2d1, a first slide rail 2d2, a first slide block 2d3 and a first relay roller 2d4, the first frame 2d1 slides along the height direction of the first lifting support 2a, the first frame 2d1 is provided with a first slide rail 2d2, the first slide rail 2d2 is slidably connected with a first slide block 2d3, one end surface of the first slide block 2d3 is rotatably connected with a plurality of first relay rollers 2d4 with equal intervals, a gap between adjacent second buffer rollers 1f 6342 is provided for the first relay roller 2d4 to pass through, a gap between adjacent second transition rollers 2i5 is provided for the first relay roller 2d4 to pass through, the second relay station 2h includes a second frame 2h4, a second slide rail 2h2, a second slide block 2h3 and a second relay roller 462 h4, the second relay roller 2h 462 h is provided with a second slide rail 2h 585, the second slide rail 2h2 is connected with a second slide block 2h3 in a sliding manner, one end face of the second slide block 2h3 is connected with a plurality of second transit rollers 2h4 with equal intervals in a rotating manner, a gap between every two adjacent second blanking rollers 2k5 is used for the second transit rollers 2h4 to pass through, and a gap between every two adjacent third transition rollers 2i6 is used for the second transit rollers 2h4 to pass through. When the first driving motor 2b works, the belt on the first belt transmission module 2c is driven to rotate, the first sliding block 2d3 is connected with the belt of the first belt transmission module 2c, so that the first sliding block 2d3 performs elliptic circular motion along the first slide rail 2d2 and approaches the buffer rail 1f in the process, a gap between the adjacent second buffer rollers 1f4 is used for the first transfer roller 2d4 to pass through, the blank 5 slides out of the buffer rail 1f due to motion inertia and finally falls onto the first transfer roller 2d4, the first transfer roller 2d4 is used for carrying the blank 5, a gap between the adjacent second transition rollers 2i5 is used for the first transfer roller 2d4 to pass through, and the blank 5 is transferred onto the transition table 2i by the first sliding block 2d3 in the motion process. When the second driving motor 2f works, the belt on the second belt driving module 2g is driven to rotate, the second slider 2h3 is connected with the belt of the second belt driving module 2g, so that the second slider 2h3 performs elliptic circular motion along the second slide rail 2h2, and approaches to the transition table 2i in the process, a gap between adjacent third transition rollers 2i6 is passed by the second intermediate roller 2h4, under the driving of the transition driving motor 2j, each of the first transition rollers 2i3, the second transition rollers 2i5 and the third transition rollers 2i6 rotates, so that the blank 5 passes through the second intermediate roller 2h4 from the first intermediate roller 2d4 along the first intermediate roller 2d4, the second transition rollers 2i5, the first transition rollers 2i3, the third transition rollers 2i6, enters the second intermediate roller 2h4, and the second intermediate roller 2h4 is used for carrying and carrying the blank between the second intermediate rollers 365 h4 k and the second intermediate roller 5 k, the second slider 2h3 transfers the blank 5 onto the second blanking roller 2k5 during movement. When the blanking driving belt module 2k2 works, the second blanking roller 2k5 and the first blanking roller 2k3 are driven to rotate, so that the blank 5 finally enters the stacking and blanking mechanism 4 from the second transfer roller 2h4 along the second transfer roller 2h4, the second blanking roller 2k5 and the first blanking roller 2k 3.
Referring to fig. 4, 5 and 6, the lubricant recycling mechanism 3 includes a recycling pipe 3a, a first pipe 3b, a recycling tank 3c, a second pipe 3d and a pump 3e, the recycling pipe 3a is disposed at the bottom of the blank draining mechanism 2, one end of the recycling pipe 3a is communicated with the first pipe 3b, the other end of the first pipe 3b is communicated with the recycling tank 3c, the recycling tank 3c is provided with a liquid pumping pipe 3c3, the recycling tank 3c is internally provided with a first liquid level sensor 3c1 and a second liquid level sensor 3c2, the first liquid level sensor 3c1 is located at the top of the second liquid level sensor 3c2, the outer side wall of the dip-coating tank 1a is provided with a pump 3e, and the pump 3e is communicated with the recycling tank 3c through the second pipe 3 d. The recovery pipeline 3a is used for collecting the dropped aqueous graphite lubricant, the aqueous graphite lubricant in the recovery pipeline 3a can enter the recovery box 3c along the first pipeline 3b, the first liquid level sensor 3c1 and the second liquid level sensor 3c2 are respectively high and low liquid level sensors, when the liquid level in the recovery box 3c is higher than the detection position of the first liquid level sensor 3c1, the pump machine 3e starts to work, and then when the liquid level in the recovery box 3c is lower than the detection position of the second liquid level sensor 3c2, the pump machine 3e stops working, and the pump machine 3e sucks the aqueous graphite lubricant in the recovery box 3c through the second pipeline 3d to dip-coat the aqueous graphite lubricant in the recovery box 3c into the tank 1a for recycling.
Referring to fig. 13 and 14, the stacking and blanking mechanism 4 includes a support table 4a, a material pushing cylinder 4b, a blank fixture 4c, a first screw rod sliding table 4d, a second screw rod sliding table 4e, a pneumatic clamping jaw 4f, a blanking sliding table 4g and a stacking box 4h, the support table 4a is disposed on one side of the blanking table 2k away from the second lifting bracket 2e, the material pushing cylinder 4b is disposed on one end of the support table 4a close to the blanking table 2k, the blank fixture 4c is disposed beside an output end of the material pushing cylinder 4b, the blank fixture 4c includes a fixed plate 4c1, a sliding protrusion 4c2 and a sliding plate 4c3, the sliding plate 4c3 is slidably connected on the fixed plate 4c1, the sliding protrusion 4c2 with a space is disposed on the sliding plate 4c3, the first screw rod sliding table 4d is disposed on the support table 4a, the first screw rod sliding table 4d is disposed on a side of the blank fixture 4c, the second screw rod sliding table, second lead screw slip table 4e goes up sliding connection and has pneumatic clamping jaw 4f, is equipped with feed opening 4a1 on the supporting bench 4a, and feed opening 4a1 bottom is equipped with unloading slip table 4g, and the output of unloading slip table 4g is equipped with pile box 4 h. The blank jig 4c is used for placing the blank 5, when the material pushing cylinder 4b works, the blank 5 can be pushed out, the pneumatic clamping jaw 4f can pick up the blank conveniently, after the position of the pneumatic clamping jaw 4f is adjusted through the first screw rod sliding table 4d and the second screw rod sliding table 4e, the blank 5 is picked up to the blanking port 4a1 by the pneumatic clamping jaw 4f, the blank 5 is loosened, and the blank 5 enters the stacking box 4h along the blanking sliding table 4 g.
The working principle of the invention is as follows: firstly, putting a preheated blank 5 into a blank dip-coating mechanism 1, completely soaking the blank 5 in an aqueous graphite lubricant, completing an automatic dip-coating process of the aqueous graphite lubricant in the blank dip-coating mechanism 1, then conveying the blank 5 to a blank draining mechanism 2 by the blank dip-coating mechanism 1, draining the aqueous graphite lubricant remained on the blank 5 after a series of conveying processes of the blank draining mechanism 2, enabling the aqueous graphite lubricant falling from the blank 5 to fall into a lubricant recovery mechanism 3 and be recovered by the lubricant recovery mechanism 3, enabling the lubricant recovery mechanism 3 to reflux the aqueous graphite lubricant into the blank dip-coating mechanism 1 for recycling the aqueous graphite lubricant, conveying the blank 5 to an output end by the blank draining mechanism 2, receiving the blank 5 from the blank draining mechanism 2 by a stacking and blanking mechanism 4, the blanking process of the blank 5 is performed, and the blank 5 is automatically stacked in the process.
This dip-coating emollient equipment satisfies automatic coating emollient and the driping raffinate process to auto wheel balancing piece blank, in order to carry out subsequent extrusion process, through having set up blank driping mechanism 2, 2d go up and down at first transfer station, transition platform 2i transports, 2h go up and down in the second transfer station and the transportation process of unloading platform 2k, can fully driping remaining aqueous graphite emollient on the blank 5, emollient recovery mechanism 3 gets into in blank dip-coating mechanism 1 with aqueous graphite emollient backward flow again, carry out aqueous graphite emollient's cyclic utilization, whole process degree of automation is high, make the auto wheel balancing piece performance of preparation better.
Claims (6)
1. An automatic lubricant dip-coating device for automobile wheel balance blocks is characterized by comprising:
the blank dip-coating mechanism (1) is filled with aqueous graphite lubricant diluted by 1: 1, and the preheated blank (5) is soaked in the aqueous graphite lubricant to carry out the subsequent extrusion process;
the blank draining mechanism (2) is arranged on the side part of the blank dip-coating mechanism (1), and the input end of the blank draining mechanism (2) is connected with the output end of the blank dip-coating mechanism (1) and is used for draining the soaked blank (5), transferring the blank (5) and draining the residual aqueous graphite lubricant on the blank (5) in the process of transferring the blank (5);
the lubricant recovery mechanism (3) is arranged at the bottom of the blank draining mechanism (2) and is used for recovering the water aqua graphite lubricant drained and thrown off by the blank draining mechanism (2) and refluxing the water aqua graphite lubricant into the blank dip-coating mechanism (1) for recycling the water aqua graphite lubricant;
the stacking and blanking mechanism (4) is arranged on the side part of the blank draining mechanism (2), and the input end of the stacking and blanking mechanism (4) is connected with the output end of the blank draining mechanism (2) and is used for completing the blanking process of the blank (5) after residual liquid is drained and automatically stacking;
the blank dip-coating mechanism (1) comprises a dip-coating box (1 a), a feeding pipeline (1 b), a transfer driving motor (1 c), a transfer gear set (1 d), a feeding guide plate (1 e) and a buffering track (1 f), wherein the water aqua graphite lubricant diluted according to the ratio of 1: 1 is contained in the dip-coating box (1 a), the feeding pipeline (1 b) and the buffering track (1 f) are respectively arranged at two ends of the dip-coating box (1 a), the transfer driving motor (1 c) is arranged on the outer side wall of the dip-coating box (1 a), the transfer driving motor (1 c) is in transmission connection with the transfer gear set (1 d) arranged in the dip-coating box (1 a), the transfer gear set (1 d) is gradually inclined upwards from the feeding pipeline (1 b) to the feeding guide plate (1 e), one end, close to the feeding guide plate (1 e), of the transfer gear set (1 d) is higher than the liquid level of the water aqua graphite lubricant, the top of the transfer gear set (1 d) is provided with a pair of feeding guide plates (1 e), and the distance between the two feeding guide plates (1 e) gradually decreases from the feeding pipeline (1 b) to the feeding guide plates (1 e);
the bottom of the dip-coating box (1 a) is provided with a stirring driving motor (1 g), and an output shaft of the stirring driving motor (1 g) penetrates through the dip-coating box (1 a) and is in transmission connection with a stirring shaft (1 h);
the buffer rail (1 f) comprises a first supporting plate (1 f 1), a first buffer roller (1 f 2), a second supporting plate (1 f 3) and a second buffer roller (1 f 4), the first support plate (1 f 1) and the second support plate (1 f 3) are fixed on the outer side wall of the dip-coating box (1 a), the first support plate (1 f 1) and the second support plate (1 f 3) are arranged in parallel, the first supporting plate (1 f 1) is longer than the second supporting plate (1 f 3) in arrangement, a plurality of first buffer rollers (1 f 2) with equal intervals are rotatably connected between the first supporting plate (1 f 1) and the second supporting plate (1 f 3), the first buffer rollers (1 f 2) are arranged close to the dip-coating box (1 a), a part, which is longer than the second supporting plate (1 f 3), of the first supporting plate (1 f 1) is rotatably connected with a plurality of second buffer rollers (1 f 4) with equal intervals, and the intervals between the second buffer rollers (1 f 4) are larger than the intervals between the first buffer rollers (1 f 2);
the blank draining mechanism (2) comprises a first lifting support (2 a), a first driving motor (2 b), a first belt transmission module (2 c), a first transfer platform (2 d), a second lifting support (2 e), a second driving motor (2 f), a second belt transmission module (2 g), a second transfer platform (2 h), a transition platform (2 i), a transition driving motor (2 j), a blanking platform (2 k) and a blanking guide roller (2 l), wherein the first lifting support (2 a) is arranged on the side part of the buffering track (1 f), the first driving motor (2 b) is arranged on the first lifting support (2 a), the first driving motor (2 b) is in transmission connection with the first belt transmission module (2 c), the first transfer platform (2 d) is arranged on the side part of the first belt transmission module (2 c), and the first transfer platform (2 d) is in sliding connection with the first lifting support (2 a), the sliding mechanism slides along the height direction of a first lifting support (2 a), a first transfer platform (2 d) is matched with a buffering track (1 f), the input end of the first transfer platform (2 d) is connected with the output end of the buffering track (1 f), the side part of the first lifting support (2 a) is provided with a second lifting support (2 e), the second lifting support (2 e) is provided with a second driving motor (2 f), the second driving motor (2 f) is in transmission connection with a second belt transmission module (2 g), the side part of the second belt transmission module (2 g) is provided with a second transfer platform (2 h), the second transfer platform (2 h) is in sliding connection with the second lifting support (2 e) and slides along the height direction of the second lifting support (2 e), a transition platform (2 i) is arranged between the first lifting support (2 a) and the second lifting support (2 e), the transition table (2 i) is arranged at the top ends of the first lifting support (2 a) and the second lifting support (2 e), the transition driving motor (2 j) is arranged at the top of the transition table (2 i), the output end of the transition driving motor (2 j) is in transmission connection with the transition table (2 i), the transition table (2 i) is matched with the first transfer table (2 d), the input end of the transition table (2 i) is connected with the output end of the first transfer table (2 d), the second transfer table (2 h) is matched with the transition table (2 i), the input end of the second transfer table (2 h) is connected with the output end of the transition table (2 i), the blanking table (2 k) is arranged at the bottom of the second lifting support (2 e), the blanking table (2 k) is matched with the second transfer table (2 h), the input end of the blanking table (2 k) is connected with the output end of the second transfer table (2 h), the output end of the blanking table (2 k) is provided with a pair of blanking guide rollers (2 l), and the distance between the two blanking guide rollers (2 l) is gradually reduced from the input end of the blanking table (2 k) to the output end of the blanking table (2 k).
2. The automatic lubricant dipping and coating device for the vehicle wheel balancing weight according to claim 1, wherein the transition table (2 i) comprises a third supporting plate (2 i 1), a transition driving belt module (2 i 2), a first transition roller (2 i 3), a fourth supporting plate (2 i 4), a second transition roller (2 i 5) and a third transition roller (2 i 6), the third supporting plate (2 i 1) and the fourth supporting plate (2 i 4) are positioned at the top ends of a first lifting bracket (2 a) and a second lifting bracket (2 e), the third supporting plate (2 i 1) and the fourth supporting plate (2 i 4) are arranged in parallel, two ends of the third supporting plate (2 i 1) extend out of the fourth supporting plate (2 i 4), a plurality of first transition rollers (2 i 3) with equal intervals are rotatably connected between the third supporting plate (2 i 1) and the fourth supporting plate (2 i 4), and a plurality of rotating intervals of the first transition rollers (2 i 3) are connected to the third supporting plate (2 i 1) close to one end of the first lifting bracket (2 i 4) Equal second transition roller (2 i 5), the one end rotation that third backup pad (2 i 1) are close to second lifting support (2 e) is connected with a plurality of intervals and equals third transition roller (2 i 6), interval between second transition roller (2 i 5) is greater than interval between first transition roller (2 i 3), interval between third transition roller (2 i 6) is greater than interval between first transition roller (2 i 3), be equipped with on third backup pad (2 i 1) transition driving belt module (2 i 2), the output and the transmission of transition driving belt module (2 i 2) of transition driving motor (2 j) are connected, and transition driving belt module (2 i 2) drive first transition roller (2 i 3), second transition roller (2 i 5) and third transition roller (2 i 6) rotate.
3. The automatic lubricant dipping device for the vehicle wheel balancing weight according to claim 2, wherein the blanking table (2 k) comprises a fifth supporting plate (2 k 1), a blanking transmission belt module (2 k 2), a first blanking roller (2 k 3), a sixth supporting plate (2 k 4), a second blanking roller (2 k 5), a supporting chassis (2 k 6) and a deviation-correcting driving cylinder (2 k 7), the fifth supporting plate (2 k 1) and the sixth supporting plate (2 k 4) are positioned on one side of the second lifting bracket (2 e) far away from the first lifting bracket (2 a), the fifth supporting plate (2 k 1) is arranged in parallel with the sixth supporting plate (2 k 4), one end of the fifth supporting plate (2 k 1) close to the second lifting bracket (2 e) extends out of the sixth supporting plate (2 k 4), and a plurality of blanking rollers (3) with equal spacing are rotatably connected between the fifth supporting plate (2 k 1) and the sixth supporting plate (2 k 4), one end of a fifth supporting plate (2 k 1) extending out of a sixth supporting plate (2 k 4) is rotatably connected with a plurality of second blanking rollers (2 k 5) with equal intervals, the interval between the second blanking rollers (2 k 5) is larger than the interval between the first blanking rollers (2 k 3), the fifth supporting plate (2 k 1) is provided with a blanking transmission belt module (2 k 2) for driving the first blanking roller (2 k 3) and the second blanking roller (2 k 5) to rotate, the bottom of the first blanking roller (2 k 3) is provided with a supporting underframe (2 k 6), the supporting underframe (2 k 6) is provided with a deviation rectifying driving cylinder (2 k 7), the output end of the driving deviation rectifying cylinder (2 k 7) is provided with a pair of first deviation rectifying columns (2 k 8) and a pair of second deviation rectifying columns (2 k 9), a certain gap is formed between the two first deviation rectifying columns (2 k 8) and penetrates through one of the first blanking rollers (2 k 3), and the second deviation rectifying column (9) is positioned at the side part of the first deviation rectifying column (2 k 8), a certain gap exists between the two second deviation rectifying columns (2 k 9), and the two second deviation rectifying columns pass through the first blanking rollers (2 k 3) through which the two first deviation rectifying columns (2 k 8) pass.
4. The automatic lubricant dip-coating device for the vehicle wheel balance weight according to claim 3, wherein the first transfer table (2 d) comprises a first frame (2 d 1), a first slide rail (2 d 2), a first slide block (2 d 3) and a first transfer roller (2 d 4), the first frame (2 d 1) slides along the height direction of the first lifting bracket (2 a), the first slide rail (2 d 2) is arranged on the first frame (2 d 1), the first slide block (2 d 3) is slidably connected on the second slide rail (2 d 2), a plurality of first transfer rollers (2 d 4) with equal intervals are rotatably connected on one end face of the first slide block (2 d 3), gaps between adjacent second buffer rollers (1 f 4) are used for the first transfer roller (2 d 4) to pass through, and gaps between adjacent second transfer rollers (2 i 5) are used for the first transfer roller (2 d 4) to pass through, the second transfer table (2 h) comprises a second frame (2 h 1), a second sliding rail (2 h 2), a second sliding block (2 h 3) and a second transfer roller (2 h 4), the second frame (2 h 1) slides in the height direction of the first lifting support (2 a), the second sliding rail (2 h 2) is arranged on the second frame (2 h 1), the second sliding rail (2 h 2) is connected with the second sliding block (2 h 3) in a sliding mode, one end face of the second sliding block (2 h 3) is rotatably connected with the second transfer roller (2 h 4) with a plurality of equal intervals, gaps between adjacent second blanking rollers (2 k 5) are used for the second transfer roller (2 h 4) to pass through, and gaps between adjacent third transfer rollers (2 i 6) are used for the second transfer roller (2 h 4) to pass through.
5. The automatic lubricant dipping and coating device for the automobile wheel balance weight according to claim 4, wherein the lubricant recycling mechanism (3) comprises a recycling pipeline (3 a), a first pipeline (3 b), a recycling tank (3 c), a second pipeline (3 d) and a pump (3 e), the recycling pipeline (3 a) is arranged at the bottom of the blank draining mechanism (2), one end of the recycling pipeline (3 a) is communicated with the first pipeline (3 b), the other end of the first pipeline (3 b) is communicated with the recycling tank (3 c), a liquid pumping pipeline (3 c 3) is arranged on the recycling tank (3 c), a first liquid level sensor (3 c 1) and a second liquid level sensor (3 c 2) are arranged inside the recycling tank (3 c), the first liquid level sensor (3 c 1) is arranged at the top of the second liquid level sensor (3 c 2), and the pump (3 e) is arranged on the outer side wall of the dipping and coating tank (1 a), the pump (3 e) is communicated with the recovery tank (3 c) through the second pipeline (3 d).
6. The automatic lubricant dipping and coating device for the automobile wheel balance block according to claim 5, wherein the stacking and blanking mechanism (4) comprises a supporting table (4 a), a material pushing cylinder (4 b), a blank fixture (4 c), a first screw rod sliding table (4 d), a second screw rod sliding table (4 e), a pneumatic clamping jaw (4 f), a blanking sliding table (4 g) and a stacking box (4 h), the supporting table (4 a) is arranged on one side of the blanking table (2 k) far away from the second lifting support (2 e), one end of the supporting table (4 a) close to the blanking table (2 k) is provided with the material pushing cylinder (4 b), the blank fixture (4 c) is arranged beside the output end of the material pushing cylinder (4 b), the blank fixture (4 c) comprises a fixing plate (4 c 1), a sliding bulge (4 c 2) and a sliding plate (4 c 3), the sliding plate (4 c 3) is connected on the fixing plate (4 c 1) in a sliding manner, be equipped with on sliding plate (4 c 3) and have the interval slide arch (4 c 2), be equipped with on supporting bench (4 a) first lead screw slip table (4 d), first lead screw slip table (4 d) are located the lateral part of blank tool (4 c), and sliding connection has on first lead screw slip table (4 d) second lead screw slip table (4 e), sliding connection has on second lead screw slip table (4 e) pneumatic clamping jaw (4 f), are equipped with feed opening (4 a 1) on supporting bench (4 a), and feed opening (4 a 1) bottom is equipped with unloading slip table (4 g), the output of unloading slip table (4 g) is equipped with pile box (4 h).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010329541.4A CN111420842B (en) | 2020-04-24 | 2020-04-24 | Automatic lubricant dip-coating equipment for automobile wheel balance block |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010329541.4A CN111420842B (en) | 2020-04-24 | 2020-04-24 | Automatic lubricant dip-coating equipment for automobile wheel balance block |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN111420842A CN111420842A (en) | 2020-07-17 |
| CN111420842B true CN111420842B (en) | 2021-03-02 |
Family
ID=71554486
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010329541.4A Active CN111420842B (en) | 2020-04-24 | 2020-04-24 | Automatic lubricant dip-coating equipment for automobile wheel balance block |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111420842B (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112303466A (en) * | 2020-11-02 | 2021-02-02 | 广东电网有限责任公司 | An electrified lubricating oil device for overhead line operating mechanism |
| CN113385359B (en) * | 2021-06-21 | 2024-02-27 | 安徽省无为天成纺织有限公司 | Pipelined spinning rod body oiling protector |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2003293172A (en) * | 2002-04-05 | 2003-10-15 | Kyowa Kogyo Kk | Method and apparatus for coating application of glaze |
| CN201744430U (en) * | 2010-05-26 | 2011-02-16 | 华锋精密机械有限公司 | Passive component coating machine |
| CN204638453U (en) * | 2015-05-20 | 2015-09-16 | 绵阳市万欣测控技术有限公司 | A kind of circulation automatic infiltration oil machine antirust for stretcher |
| CN206028074U (en) * | 2016-08-23 | 2017-03-22 | 江阴和港机械有限公司 | Oil immersion machine |
| CN206215461U (en) * | 2016-11-11 | 2017-06-06 | 重庆厚辉汽车配件有限公司 | A kind of automatic painting device |
| CN207430606U (en) * | 2014-09-02 | 2018-06-01 | 伊扎维克技术有限责任公司 | Device for obtaining nanostructured coatings on solid surfaces |
| CN208161991U (en) * | 2018-02-07 | 2018-11-30 | 江苏沃维斯智能工业有限公司 | Three station elevating mechanism of separator |
| CN110355532A (en) * | 2019-07-26 | 2019-10-22 | 朱林辉 | A kind of bearing manufacturing method |
| CN110860426A (en) * | 2019-11-28 | 2020-03-06 | 奥林汽车零部件(常熟)有限公司 | Automatic immersion oil drying device of stamping workpiece |
| CN210252963U (en) * | 2019-07-04 | 2020-04-07 | 宁夏瑞鑫泽塑料工贸有限公司 | Special production facility of circulating pipe high density |
-
2020
- 2020-04-24 CN CN202010329541.4A patent/CN111420842B/en active Active
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2003293172A (en) * | 2002-04-05 | 2003-10-15 | Kyowa Kogyo Kk | Method and apparatus for coating application of glaze |
| CN201744430U (en) * | 2010-05-26 | 2011-02-16 | 华锋精密机械有限公司 | Passive component coating machine |
| CN207430606U (en) * | 2014-09-02 | 2018-06-01 | 伊扎维克技术有限责任公司 | Device for obtaining nanostructured coatings on solid surfaces |
| CN204638453U (en) * | 2015-05-20 | 2015-09-16 | 绵阳市万欣测控技术有限公司 | A kind of circulation automatic infiltration oil machine antirust for stretcher |
| CN206028074U (en) * | 2016-08-23 | 2017-03-22 | 江阴和港机械有限公司 | Oil immersion machine |
| CN206215461U (en) * | 2016-11-11 | 2017-06-06 | 重庆厚辉汽车配件有限公司 | A kind of automatic painting device |
| CN208161991U (en) * | 2018-02-07 | 2018-11-30 | 江苏沃维斯智能工业有限公司 | Three station elevating mechanism of separator |
| CN210252963U (en) * | 2019-07-04 | 2020-04-07 | 宁夏瑞鑫泽塑料工贸有限公司 | Special production facility of circulating pipe high density |
| CN110355532A (en) * | 2019-07-26 | 2019-10-22 | 朱林辉 | A kind of bearing manufacturing method |
| CN110860426A (en) * | 2019-11-28 | 2020-03-06 | 奥林汽车零部件(常熟)有限公司 | Automatic immersion oil drying device of stamping workpiece |
Also Published As
| Publication number | Publication date |
|---|---|
| CN111420842A (en) | 2020-07-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111906531B (en) | Electric locomotive wheel drive unit assembly line | |
| CN108481000A (en) | Full-automatic uncoiling leveling laser cutting blanking automatic stacking intelligent manufacturing production line | |
| CN201931321U (en) | Automatic feeding and discharging device of sheet processing equipment | |
| CN207464681U (en) | Fully automatic uncoiling and leveling laser cutting blanking automatic stacking intelligent manufacturing production line | |
| CN111420842A (en) | Automatic lubricant dip-coating equipment for automobile wheel balance block | |
| CN110040415B (en) | Integrated laser automatic feeding and discharging mechanism and method thereof | |
| CN211895211U (en) | Unpowered automatic material transfer device | |
| CN1057058C (en) | Web bundle transporting belt equiped with reciprocating moving crane with elevating mechanism | |
| CN111572871A (en) | New energy automobile battery packing transportation equipment | |
| CN102976108A (en) | Concrete block stacker | |
| CN114798944B (en) | Automatic bending production line | |
| CN112027550A (en) | A laborsaving type handling device for material transport uses | |
| CN110482153A (en) | A kind of lead pig automatic conveying device | |
| CN205733831U (en) | Hall door flexible production line | |
| CN214189675U (en) | Double-deck material transport vechicle | |
| CN112743340B (en) | Production line for machining die-casting aluminum box body | |
| CN210214137U (en) | a destacker | |
| CN219004970U (en) | Scissor fork type lifting sucker tool | |
| CN215625731U (en) | Delivery device for gilding press | |
| CN218200599U (en) | Electric lifting roller conveyor for lithium battery material frame | |
| CN205973630U (en) | Multi -functional stacker | |
| JP3488596B2 (en) | Iron stacking equipment | |
| CN217229011U (en) | Stacking machine for stacking standard supporting pieces | |
| CN215706740U (en) | Conveyer is used in steel pipe production and processing | |
| CN205602643U (en) | Novel automatic turn -over machine of steel sheet |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| TA01 | Transfer of patent application right | ||
| TA01 | Transfer of patent application right |
Effective date of registration: 20210210 Address after: No. 42-1, Xi'ao Road, Shuangyu street, Lucheng District, Wenzhou City, Zhejiang Province 325000 Applicant after: Zheng Lanjie Address before: No.299 Xuefu Road, Wuxing District, Huzhou City, Zhejiang Province Applicant before: Zeng Yonghong |
|
| GR01 | Patent grant | ||
| GR01 | Patent grant |