CN111300787A - Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit - Google Patents
Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit Download PDFInfo
- Publication number
- CN111300787A CN111300787A CN201911298189.6A CN201911298189A CN111300787A CN 111300787 A CN111300787 A CN 111300787A CN 201911298189 A CN201911298189 A CN 201911298189A CN 111300787 A CN111300787 A CN 111300787A
- Authority
- CN
- China
- Prior art keywords
- edge
- cutter
- core
- core pulling
- slitting
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/03—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor characterised by the shape of the extruded material at extrusion
- B29C48/07—Flat, e.g. panels
- B29C48/08—Flat, e.g. panels flexible, e.g. films
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/001—Combinations of extrusion moulding with other shaping operations
- B29C48/0022—Combinations of extrusion moulding with other shaping operations combined with cutting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/275—Recovery or reuse of energy or materials
- B29C48/277—Recovery or reuse of energy or materials of materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/28—Storing of extruded material, e.g. by winding up or stacking
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
Abstract
本发明涉及一种塑料挤出流延薄膜机组在线切边吸边、分切抽芯装置,其包括设置在机架上的负压风管、与负压风管通过软连接管连通的风嘴以及与安装在机架上与风嘴位置相对应的边部切刀,所述边部切刀位于机架的两端,在两个所述边部切刀之间设置有抽芯装置;本发明通过在边部切刀的位置对应的增加负压的端部风嘴,将薄膜在被切割过程中产生的废边迅速的吸走,不会残留在生产现场,保持现场的洁净程度以及产品质量。
The invention relates to an on-line edge trimming and edge suction, slitting and core pulling device of a plastic extrusion casting film unit, which comprises a negative pressure air duct arranged on a frame and an air nozzle communicated with the negative pressure air duct through a flexible connecting pipe and a side cutter installed on the frame corresponding to the position of the air nozzle, the side cutter is located at both ends of the frame, and a core pulling device is arranged between the two side cutters; The invention uses the end tuyere corresponding to increase the negative pressure at the position of the edge cutter, so that the waste edge generated during the cutting process of the film can be quickly sucked away, and it will not remain in the production site, maintaining the cleanliness of the site and the product. quality.
Description
技术领域technical field
本发明涉及塑料薄膜生产设备领域,具体是一种塑料挤出流延薄膜机组在线切边吸边、分切抽芯装置。The invention relates to the field of plastic film production equipment, in particular to a device for on-line edge trimming, edge suction, slitting and core pulling of a plastic extrusion casting film unit.
背景技术Background technique
薄膜在生产过程中,开始的薄膜是宽度比较大的连续薄膜,由于生产工艺的因素需要将薄膜边缘处切除。同时在实际需求中,往往会用到宽度较小的薄膜或直接成品,这样就需要在薄膜生产过程中将其切开分隔成较小宽的薄膜,然后缠绕在纸管上,目前设备采用的是弧形辊,其自带弧度,利用弧形辊弧度和拉伸来调整膜卷在纸管上的距离,也就是相邻两段卷膜边缘之间的需要保持一定距离,避免膜与膜边缘之间的接触。同时由于拉伸的因素薄膜也会受到影响。In the production process of the film, the starting film is a continuous film with a relatively large width, and the edge of the film needs to be cut off due to the factors of the production process. At the same time, in actual demand, films with smaller widths or direct finished products are often used, so it needs to be cut and separated into smaller width films during the production process of the film, and then wound on the paper tube. It is an arc-shaped roller with its own arc. The arc-shaped roller arc and stretching are used to adjust the distance of the film roll on the paper tube. contact between edges. At the same time, the film will also be affected due to the stretching factor.
发明内容SUMMARY OF THE INVENTION
本发明所要解决的技术问题一种在薄膜生产过程中对薄膜的边缘进行切除并且对薄膜分割成若干份宽度较窄的塑料挤出流延薄膜机组在线切边吸边、分切抽芯装置The technical problem to be solved by the present invention is an on-line cutting edge suction, slitting core pulling device for cutting the edge of the film and dividing the film into several narrow width plastic extrusion casting film units in the film production process
本发明所采用的技术方案是:一种塑料挤出流延薄膜机组在线切边吸边、分切抽芯装置,其包括设置在机架上的负压风管、与负压风管通过软连接管连通的风嘴以及与安装在机架上与风嘴位置相对应的边部切刀,所述边部切刀位于机架的两端,在两个所述边部切刀之间设置有抽芯装置。The technical scheme adopted in the present invention is: an on-line edge trimming and edge suction, slitting and core pulling device of a plastic extrusion cast film unit, which comprises a negative pressure air duct arranged on the frame, and a negative pressure air duct through a soft A tuyere communicated with the connecting pipe and an edge cutter installed on the frame corresponding to the position of the tuyere, the edge cutters are located at both ends of the frame, and are arranged between the two edge cutters There is a core pulling device.
进一步的,所述风嘴包括通过风嘴支架安装在机架上并且与边部切刀位置相对应的端部风嘴。Further, the tuyere includes an end tuyere which is mounted on the frame through a tuyere bracket and corresponds to the position of the edge cutter.
进一步的,所述风嘴支架包括通过上安装座设置在机架上的竖杆以及通过下安装座安装在竖杆上的横杆,在所述横杆的端部设置有用于与风嘴连接的抱箍。Further, the tuyere bracket includes a vertical rod installed on the frame through the upper mounting seat and a horizontal rod installed on the vertical rod through the lower mounting seat, and an end of the horizontal rod is provided for connecting with the tuyere. hoop.
进一步的,所述上安装座固定在机架上,竖杆滑动连接套置在上安装座内,下安装座固定安装在竖杆的底部,横杆滑动连接套置在下安装座内,在上安装座和下安装座上均设置有用于锁紧竖杆和横杆的锁紧螺栓。Further, the upper installation seat is fixed on the frame, the vertical rod sliding connection is sleeved in the upper installation seat, the lower installation seat is fixedly installed at the bottom of the vertical rod, the horizontal rod sliding connection is sleeved in the lower installation seat, and the upper The mounting seat and the lower mounting seat are provided with locking bolts for locking the vertical rod and the horizontal rod.
进一步的,所述抽芯装置包括设置在两个所述边部切刀之间的抽芯切刀以及与抽芯切刀的位置相对应的抽芯风嘴。Further, the core pulling device includes a core pulling cutter disposed between the two edge cutters and a core pulling air nozzle corresponding to the position of the core pulling cutter.
进一步的,所述抽芯风嘴通过软连接管与负压风管联通。Further, the core pulling air nozzle is communicated with the negative pressure air duct through a flexible connecting pipe.
进一步的,所述抽芯切刀包括刀杆以及设置在刀杆下端的刀片。Further, the core-pulling cutter includes a cutter bar and a blade disposed at the lower end of the cutter bar.
进一步的,所述刀片为两个且分别设置在刀杆的两侧。Further, there are two blades and they are respectively arranged on both sides of the blade shank.
进一步的,在所述刀片与刀杆之间设置有调距压片。Further, a distance-adjusting pressing piece is arranged between the blade and the cutter bar.
进一步的,在机架上设置有支撑杠,所述边部切刀和抽芯切刀滑动设置在支撑杠上;Further, a support bar is provided on the frame, and the edge cutter and the core-pulling cutter are slidably arranged on the support bar;
在支撑杠上设置有标尺,边部切刀和抽芯切刀的顶部顶端呈尖状并且与标尺的位置相对应。A ruler is arranged on the support bar, and the top ends of the edge cutter and the core-pulling cutter are pointed and correspond to the position of the ruler.
本发明的积极效果为:本发明通过在边部切刀的位置对应的增加负压的端部风嘴,将薄膜在被切割过程中产生的废边迅速的吸走,不会残留在生产现场,保持现场的洁净程度以及产品质量。The positive effects of the present invention are: the present invention quickly sucks away the waste edges generated during the cutting process of the film by means of the end air nozzles with correspondingly increased negative pressure at the positions of the edge cutters, and will not remain on the production site , to maintain the cleanliness of the site and product quality.
在两个边部切刀之间增加抽芯切刀,在卷膜的过程中将薄膜分隔成若干段宽度较小的薄膜,然后再卷到纸管上,抽芯切刀采用双切刀设计,利用抽芯风嘴将两个抽芯切刀切下的薄膜部分吸走,使得纸管上的膜卷端面非常整齐。避免使用弧形辊而导致薄膜受到拉伸影响,膜卷端面参差不齐。A core-pulling cutter is added between the two edge cutters, and the film is divided into several sections with smaller widths during the film rolling process, and then rolled onto the paper tube. The core-pulling cutter adopts a double cutter design , Use the core-pulling air nozzle to suck away the film part cut by the two core-pulling cutters, so that the end face of the film roll on the paper tube is very neat. Avoid the use of curved rolls to cause the film to be affected by stretching, and the end face of the film roll is uneven.
同时边部切刀、抽芯切刀、端部风嘴以及抽芯风嘴的位置可以分别进行调节,可以满足多种不同宽度尺寸的薄膜切割工作。At the same time, the positions of the edge cutter, the core-pulling cutter, the end air nozzle and the core-pulling air nozzle can be adjusted separately, which can meet the film cutting work of various widths and sizes.
附图说明Description of drawings
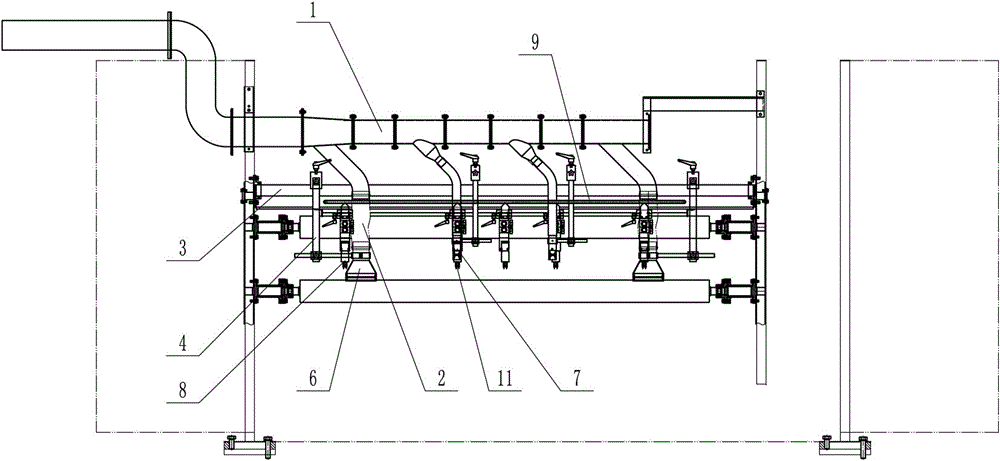
图1为本发明结构示意图;Fig. 1 is the structural representation of the present invention;
图2为本发明风嘴结构示意图;Fig. 2 is the structure schematic diagram of the tuyere of the present invention;
图3为本发明风嘴支架结构示意图;Fig. 3 is the structure schematic diagram of the tuyere bracket of the present invention;
图4为本发明抽芯切刀结构示意图。FIG. 4 is a schematic view of the structure of the core-pulling cutter of the present invention.
具体实施方式Detailed ways
如附图1-4所示,本发明包括横置在机架上的负压风管1、倾斜设置并且与负压风管1连通的通风管、与通风管通过软连接管2连通的风嘴以及与安装在第二支撑杠15上与风嘴位置相对应的边部切刀8,所述边部切刀8位于第二支撑杠15的两端用于切除薄膜两端的边缘部分,即通风管将软连接管2与负压风管1连通,所述切刀8的位置与导辊5的位置相对应,利用负压将切边过程中产生的废边快速吸走。As shown in the accompanying drawings 1-4, the present invention includes a negative pressure air duct 1 placed horizontally on the frame, a ventilation duct arranged obliquely and communicated with the negative pressure air duct 1, and an air duct communicated with the air duct through a flexible connecting
在两个所述边部切刀8之间设置有抽芯装置,用于将较宽的薄膜切割成若干个较窄的薄膜。A core pulling device is arranged between the two
风嘴包括通过风嘴支架4固定并且与边部切刀8位置相对应的端部风嘴6。The tuyere includes an
在机架上设置有第一支撑杠3,所述端部风嘴通过风嘴支架4安装在第一支撑杠3上;所述风嘴支架4包括通过套装在第一支撑杠3上的上安装座402以及滑动连接在上安装座的竖杆401以及通过下安装座405安装在竖杆401上的横杆403,在所述横杆403的端部设置有用于与风嘴连接的抱箍404。所述上安装座402套装在第一支撑杠3上,竖杆401滑动连接套置在上安装座402内,下安装座405套装在竖杆401的底部,横杆403滑动连接套置在下安装座405内,在上安装座402和下安装座405上均设置有用于锁紧竖杆401和横杆403的锁紧螺栓。A
端部风嘴可以通过风嘴支架4实现横向和竖向的移动,以满足不同尺寸要求的切边工作。The end tuyere can be moved horizontally and vertically through the
所述抽芯装置包括设置在两个所述边部切刀8之间的抽芯切刀11以及与抽芯切刀11的位置相对应的抽芯风嘴7,所述抽芯风嘴7通过软连接管2与负压风管1联通。抽芯切刀11包括刀杆10以及设置在刀杆10下端的刀片12,刀片12为两个,分别设置在刀杆10的左右两端。且两个刀片12之间设置有调距压片,使两个刀片12存在间距,并且通过调整调节压片的厚度可以调整两个压片12的间距。The core-pulling device includes a core-pulling
端部风嘴6的开口面积大于抽芯风嘴7的开口面积。在薄膜挤出后由于受外界因素和自身因素的影响会有锁边装置对薄膜边缘进行快速锁边定型,这样薄膜边缘的薄膜被强行冷却定型后会与其它不被定型的薄膜不一样,所以必须要去除,而且面积比切除废边面积略大,采用大口径的端部风嘴6可以有效将这些废边吸走。The opening area of the
在卷膜的过程中将薄膜分隔成若干段宽度较小的薄膜,然后再卷到纸管上,抽芯切刀采用双切刀设计,利用抽芯风嘴将两个抽芯切刀切下的薄膜部分吸走,使得纸管上的膜卷端面非常整齐。In the process of rolling the film, the film is divided into several sections with smaller widths, and then rolled onto the paper tube. The core-pulling cutter adopts a double-cutting knife design, and the core-pulling air nozzle is used to cut the two core-pulling cutters. The film part of the film is sucked away, so that the end face of the film roll on the paper tube is very neat.
所述边部切刀8以及抽芯切刀11均通过切刀位置调整装置设置在第二支撑杠13上,第二支撑杠13安装在机架上,切刀位置调整装置包括设置在第二支撑杠13上的滑槽以及设置在滑槽上的滑块,所述滑块安装在边部切刀8或抽芯切刀11上。The
在机架上设置有标尺9,边部切刀8以及抽芯切刀11的顶端呈尖状并且与标尺9的位置相对应。利用标尺9精确计量切刀的位置,保证切割尺寸的准确性。A
以上实施例仅用以说明本发明的技术方案,而非对其限制;尽管参照前述实施例对本发明进行了详细的说明,本领域的普通技术人员应当理解:其依然可以对前述实施例所记载的技术方案进行修改,或者对其中部分技术特征进行等同替换;而这些修改或者替换,并不使相应技术方案的本质脱离本发明实施例技术方案的精神和范围。The above embodiments are only used to illustrate the technical solutions of the present invention, but not to limit them; although the present invention has been described in detail with reference to the foregoing embodiments, those of ordinary skill in the art should understand that: it can still be described in the foregoing embodiments. Modifications are made to the technical solutions of the present invention, or some technical features thereof are equivalently replaced; and these modifications or replacements do not make the essence of the corresponding technical solutions deviate from the spirit and scope of the technical solutions of the embodiments of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911298189.6A CN111300787A (en) | 2019-12-17 | 2019-12-17 | Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911298189.6A CN111300787A (en) | 2019-12-17 | 2019-12-17 | Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111300787A true CN111300787A (en) | 2020-06-19 |
Family
ID=71154429
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201911298189.6A Pending CN111300787A (en) | 2019-12-17 | 2019-12-17 | Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111300787A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114014055A (en) * | 2021-11-30 | 2022-02-08 | 新乐华宝塑料机械有限公司 | Double-four-station staggered winding machine |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN203955636U (en) * | 2014-06-19 | 2014-11-26 | 浙江绍兴华东包装有限公司 | The online dust pelletizing system of film dividing |
| CN204295757U (en) * | 2014-12-04 | 2015-04-29 | 松德机械股份有限公司 | A kind of online carving knife stripping structure |
| CN204471463U (en) * | 2015-03-12 | 2015-07-15 | 河北宏达环境工程有限公司装备制造厂 | A kind of Double Directional Cutting machine with dust exhaust apparatus for fireproof heated board |
| CN204712147U (en) * | 2015-07-02 | 2015-10-21 | 云南红塔塑胶有限公司 | A kind of plastic sheeting cutting machine with leftover material recycling device |
| CN206217009U (en) * | 2016-11-15 | 2017-06-06 | 上海大觉包装制品有限公司 | Cutting assembly for casting machine and the retracting device comprising the cutting assembly |
| CN106956299A (en) * | 2017-02-22 | 2017-07-18 | 浙江凯阳新材料股份有限公司 | A kind of thin film leftover material cuts retracting device |
| CN108408455A (en) * | 2018-02-08 | 2018-08-17 | 浙江汇锋薄膜科技有限公司 | A kind of film cutting machine that edge is anti-roll |
| CN209755325U (en) * | 2019-02-23 | 2019-12-10 | 嘉兴新安包装材料有限公司 | Film splitter |
| CN211591213U (en) * | 2019-12-17 | 2020-09-29 | 新乐华宝塑料机械有限公司 | Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit |
-
2019
- 2019-12-17 CN CN201911298189.6A patent/CN111300787A/en active Pending
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN203955636U (en) * | 2014-06-19 | 2014-11-26 | 浙江绍兴华东包装有限公司 | The online dust pelletizing system of film dividing |
| CN204295757U (en) * | 2014-12-04 | 2015-04-29 | 松德机械股份有限公司 | A kind of online carving knife stripping structure |
| CN204471463U (en) * | 2015-03-12 | 2015-07-15 | 河北宏达环境工程有限公司装备制造厂 | A kind of Double Directional Cutting machine with dust exhaust apparatus for fireproof heated board |
| CN204712147U (en) * | 2015-07-02 | 2015-10-21 | 云南红塔塑胶有限公司 | A kind of plastic sheeting cutting machine with leftover material recycling device |
| CN206217009U (en) * | 2016-11-15 | 2017-06-06 | 上海大觉包装制品有限公司 | Cutting assembly for casting machine and the retracting device comprising the cutting assembly |
| CN106956299A (en) * | 2017-02-22 | 2017-07-18 | 浙江凯阳新材料股份有限公司 | A kind of thin film leftover material cuts retracting device |
| CN108408455A (en) * | 2018-02-08 | 2018-08-17 | 浙江汇锋薄膜科技有限公司 | A kind of film cutting machine that edge is anti-roll |
| CN209755325U (en) * | 2019-02-23 | 2019-12-10 | 嘉兴新安包装材料有限公司 | Film splitter |
| CN211591213U (en) * | 2019-12-17 | 2020-09-29 | 新乐华宝塑料机械有限公司 | Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114014055A (en) * | 2021-11-30 | 2022-02-08 | 新乐华宝塑料机械有限公司 | Double-four-station staggered winding machine |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN107381177A (en) | A kind of bundling trimming device | |
| CN201890651U (en) | Film slitting device | |
| CN110815353B (en) | Edge cutting device for film layering | |
| CN205061107U (en) | Cutter mechanism of film splitter | |
| CN207001828U (en) | A kind of bundling trimming device | |
| CN211591213U (en) | Online trimming, edge sucking, slitting and core pulling device of plastic extrusion casting film unit | |
| CN209063162U (en) | A cutting device for finished waterproof coiled material | |
| CN223983889U (en) | A fabric cutting device | |
| CN219156066U (en) | Cutting device for plastic film processing | |
| CN219649185U (en) | Slitting machine for aluminum strip production | |
| CN219116781U (en) | Splitting machine for winding drum film | |
| CN211003856U (en) | On-line film slitting device of casting machine | |
| CN223948039U (en) | Sheet extruder for cup processing | |
| CN219445320U (en) | Cutting equipment is used in bubble piece production | |
| CN219234499U (en) | Fixed-length shearing mechanism for steel strip coiled material rolling production line | |
| CN109927266B (en) | Blowing mechanism of EPS sheet production system | |
| CN207643530U (en) | A kind of trimming device of cast film line | |
| CN218639717U (en) | Material cutting and folding device | |
| CN219054488U (en) | Cutting machine for napkin paper production | |
| CN223981849U (en) | An automatic following edge trimming device for a blown film machine | |
| CN221436581U (en) | Strip sheet cutting device for processing plastic products | |
| CN219751430U (en) | A plastic film cutting mechanism | |
| CN222844194U (en) | Trimming device for facial tissue production | |
| CN215478637U (en) | A slitting structure for cash register paper processing | |
| CN219095829U (en) | XPE master slice cooling traction all-in-one |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200619 |
|
| RJ01 | Rejection of invention patent application after publication |