CN111136315A - Milling cutter head and milling cutter - Google Patents
Milling cutter head and milling cutter Download PDFInfo
- Publication number
- CN111136315A CN111136315A CN202010115424.8A CN202010115424A CN111136315A CN 111136315 A CN111136315 A CN 111136315A CN 202010115424 A CN202010115424 A CN 202010115424A CN 111136315 A CN111136315 A CN 111136315A
- Authority
- CN
- China
- Prior art keywords
- milling cutter
- cutter head
- arc
- shaped
- cutting
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23C—MILLING
- B23C5/00—Milling-cutters
- B23C5/02—Milling-cutters characterised by the shape of the cutter
- B23C5/10—Shank-type cutters, i.e. with an integral shaft
- B23C5/1081—Shank-type cutters, i.e. with an integral shaft with permanently fixed cutting inserts
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23C—MILLING
- B23C2226/00—Materials of tools or workpieces not comprising a metal
- B23C2226/42—Gem, i.e. precious stone
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Milling Processes (AREA)
Abstract
The invention relates to the technical field of machining cutters, in particular to a milling cutter head and a milling cutter. This milling cutter head includes a plurality of arc sword that the end is connected in order, and the arc sword inscribe that lies in the leading side in two adjacent arc sword is in the arc sword that lies in the caudal side. A plurality of arc-shaped edges through the milling cutter head not only can process a multi-arc-shaped revolving body through one-time rotation of the milling cutter head, so that the production efficiency of the milling cutter head is improved, smooth transition is formed between the adjacent arc-shaped edges, and the production precision of the milling cutter head can be guaranteed. Thus, the milling cutter head can meet the requirement of maintaining high-efficiency production under the requirement of high precision.
Description
Technical Field
The invention relates to the technical field of machining cutters, in particular to a milling cutter head and a milling cutter.
Background
In the related art, with the increasing demand for micro-machining technology, a single spherical surface machining is not sufficient to maintain high-efficiency production with high precision. Particularly, in the fields of optical devices and electronic devices, the requirements for production efficiency and cutting accuracy are extremely high.
Therefore, it is desirable to provide a milling cutter head capable of simultaneously machining double-curved-surface rotary bodies and even multi-curved-surface rotary bodies.
Disclosure of Invention
The invention aims to provide a milling cutter head, which solves the technical problem that the single curved surface revolving body in the prior art is not enough to maintain high-efficiency production under the high-precision requirement to a certain extent.
The second purpose of the invention is to provide a milling cutter, which solves the technical problem that the single curved surface revolving body processing in the prior art is not enough to meet the requirement of maintaining high-efficiency production under the high-precision requirement to a certain extent.
In order to achieve the above object, the present invention provides the following technical solutions;
in view of the first object, the milling cutter head according to the present invention includes a plurality of arc-shaped blades connected end to end in sequence, and the arc-shaped blade located on the leading side of two adjacent arc-shaped blades is inscribed in the arc-shaped blade located on the trailing side.
In any of the above solutions, optionally, the milling cutter head further includes a straight edge, and the straight edge is connected to and tangent to the head ends of the plurality of arc-shaped edges;
the tangent line of the tail ends of the arc-shaped edges is perpendicular to the straight edge.
In any of the above technical solutions, optionally, the milling cutter head further includes a first cutter surface and a second cutter surface connected at an included angle, and the arc-shaped edge is formed at a connection portion of the first cutter surface and the second cutter surface.
In any of the above technical solutions, optionally, the milling cutter head further includes a third tool surface connected to the first tool surface at an included angle, and the third tool surface and the second tool surface are both located on the same side of the first tool surface;
the straight edge is formed at the joint of the third knife face and the first knife face.
In any of the above claims, optionally, the milling cutter head further comprises a first, second and third cut-out surface;
the first cut surface is formed by cutting off a part of the first blade surface, the second cut surface is formed by cutting off a part of the second blade surface, and the third cut surface is formed by cutting off a part of the third blade surface;
when the milling cutter head rotates, the straight blade and the plurality of arc-shaped blades rotate to form a predetermined rotation body, and the first cutting surface, the second cutting surface, the third cutting surface, and the first cutter surface, the second cutter surface, and the third cutter surface which form the first cutting surface, the second cutting surface, and the third cutting surface are all located in the predetermined rotation body.
In any of the above technical solutions, optionally, the first cut surface, the second cut surface, and the third cut surface are flat surfaces or curved surfaces.
In any of the above solutions, optionally, the milling cutter head is formed of diamond;
the arc-shaped blade is arc-shaped;
the number of the arc-shaped edges is two.
Based on the second object, the invention provides a milling cutter, which comprises the milling cutter head provided by any one of the above technical solutions.
In any of the above technical solutions, optionally, the milling cutter further includes a milling cutter handle, the milling cutter handle includes a handle body and a tool bit seat, and the milling cutter head is welded to the tool bit seat.
In any of the above technical solutions, optionally, the tool bit seat and the tool shank body are made of tungsten steel;
and/or the cutter head seat is semi-cylindrical, and the milling cutter head is welded on the plane side wall of the cutter head seat.
By adopting the technical scheme, the invention has the beneficial effects that:
the milling cutter head provided by the invention comprises a plurality of arc-shaped blades which are sequentially connected end to end, wherein the arc-shaped blade positioned on the head side of two adjacent arc-shaped blades is internally tangent to the arc-shaped blade positioned on the tail side. A plurality of arc-shaped edges through the milling cutter head not only can process a multi-arc-shaped revolving body through one-time rotation of the milling cutter head, so that the production efficiency of the milling cutter head is improved, smooth transition is formed between the adjacent arc-shaped edges, and the production precision of the milling cutter head can be guaranteed. Thus, the milling cutter head can meet the requirement of maintaining high-efficiency production under the requirement of high precision.
The milling cutter provided by the invention comprises the milling cutter head, so that all the beneficial effects realized by the milling cutter head can be realized.
Drawings
In order to more clearly illustrate the embodiments of the present invention or the technical solutions in the prior art, the drawings used in the description of the embodiments or the prior art will be briefly described below, and it is obvious that the drawings in the following description are some embodiments of the present invention, and other drawings can be obtained by those skilled in the art without creative efforts.
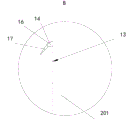
Fig. 1 is a schematic structural diagram of a milling cutter according to a second embodiment of the present invention;
FIG. 2 is an enlarged view of a portion of FIG. 1 at A;
FIG. 3 is a left side view of FIG. 1;
FIG. 4 is an enlarged view of a portion of FIG. 3 at B;
FIG. 5 is a top view of FIG. 1;
fig. 6 is a partial enlarged view of fig. 5 at C.
Icon: 10-a first curved edge; 11-a second curved edge; 12-straight edge; 13-a first blade face; 14-a second blade face; 15-a third blade face; 16-a first cut-out face; 17-a second resection surface; 18-a third resection surface; 20-a milling cutter shank; 200-a tool shank body; 201-tool tip seat.
Detailed Description
The technical solutions of the present invention will be described clearly and completely with reference to the accompanying drawings, and it should be understood that the described embodiments are some, but not all embodiments of the present invention. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
In the description of the present invention, it should be noted that the terms "center", "upper", "lower", "left", "right", "vertical", "horizontal", "inner", "outer", etc., indicate orientations or positional relationships based on the orientations or positional relationships shown in the drawings, and are only for convenience of description and simplicity of description, but do not indicate or imply that the device or element being referred to must have a particular orientation, be constructed and operated in a particular orientation, and thus, should not be construed as limiting the present invention. Furthermore, the terms "first," "second," and "third" are used for descriptive purposes only and are not to be construed as indicating or implying relative importance.
In the description of the present invention, it should be noted that, unless otherwise explicitly specified or limited, the terms "mounted," "connected," and "connected" are to be construed broadly, e.g., as meaning either a fixed connection, a removable connection, or an integral connection; can be mechanically or electrically connected; they may be connected directly or indirectly through intervening media, or they may be interconnected between two elements. The specific meanings of the above terms in the present invention can be understood in specific cases to those skilled in the art.
Example one
Referring to fig. 1 to 6, the milling cutter head provided in this embodiment includes a plurality of arc-shaped blades connected end to end in sequence, the arc-shaped blade located at the leading side of two adjacent arc-shaped blades is a first arc-shaped blade 10, and the arc-shaped blade located at the trailing side of two adjacent arc-shaped blades is a second arc-shaped blade 11. Wherein the arc-shaped edge is an elliptical or circular part.
The end of the first curved edge 10 is inscribed in the second curved edge 11. Firstly, the first arc-shaped edge 10 is inscribed in the second arc-shaped edge 11, so that the curvature radius of the first arc-shaped edge 10 is smaller than that of the second arc-shaped edge 11; secondly, the tangent point of the first arc-shaped edge 10 and the second arc-shaped edge 11 is the tail end of the first arc-shaped edge 10, namely the head end of the second arc-shaped edge 11, so that the first arc-shaped edge 10 and the second arc-shaped edge 11 can be ensured to be in smooth transition at the joint of the two; thirdly, the first arc-shaped cutting edge 10 and the second arc-shaped cutting edge 11 are connected end to form a multi-R-shaped cutting edge, so that a plurality of arc-shaped revolution bodies can be simultaneously machined by rotating the milling cutter head.
The milling cutter head in this embodiment, including a plurality of arc sword that end to end connects in order, the arc sword inscribe that is located the leading side in two adjacent arc sword is in the arc sword that is located the caudal side. A plurality of arc-shaped edges through the milling cutter head not only can process a multi-arc-shaped revolving body through one-time rotation of the milling cutter head, so that the production efficiency of the milling cutter head is improved, smooth transition is formed between the adjacent arc-shaped edges, and the production precision of the milling cutter head can be guaranteed. Thus, the milling cutter head can meet the requirement of maintaining high-efficiency production under the requirement of high precision.
In an alternative to this embodiment, which is shown in fig. 1 and 2, the milling cutter head further comprises a straight edge 12, the straight edge 12 being connected to and tangent to the head ends of the plurality of curved edges. The head ends of the arc-shaped blades are head ends when the arc-shaped blades are regarded as a whole, namely the straight blade 12 is connected and tangent with the head end of the first arc-shaped blade in the arc-shaped blades, and smooth transition of the first arc-shaped blade and the straight blade 12 at the joint of the straight blade and the straight blade can be ensured.
The tangent line perpendicular to straight sword 12 of the tail end of a plurality of arc sword to make the whole that a plurality of arc sword formed rotatory 90 for straight sword 12, and then guarantee milling cutter head at rotatory in-process, mill the work piece with the cutting edge that a plurality of arc sword and straight sword 12 are constituteed jointly.
Optionally, during the actual machining, the straight edge 12 extends parallel to the axis of rotation of the milling cutter head.
In the alternative of this embodiment, milling cutter head still includes first knife face 13 and the second knife face 14 that is the contained angle and connects, and the junction of first knife face 13 and second knife face 14 forms the arc sword, through the size of the contained angle between adjustment first knife face 13 and the second knife face 14, can adjust the sharpness and the wear resistance of arc sword. And because the first knife face 13 and the second knife face 14 are arranged in an included angle, the processing difficulty of the arc-shaped blade is facilitated to be simplified, and the controllability of the finish degree of the arc-shaped blade is improved.
In an alternative of this embodiment, as shown in fig. 6, the milling cutter head further comprises a third tool face 15 connected at an included angle to the first tool face 13, the third tool face 15 and the second tool face 14 being located on the same side of the first tool face 13; the junction of the third rake face 15 and the first rake face 13 forms a straight edge 12. The sharpness and the wear resistance of the straight edge 12 can be adjusted by adjusting the size of the included angle between the first tool face 13 and the third tool face 15. And because the first tool face 13 and the third tool face 15 are arranged in an included angle, the processing difficulty of the straight edge 12 is facilitated to be simplified, and the controllability of the finish degree of the straight edge 12 is improved.
Alternatively, the first, second and third blade surfaces 13, 14, 15 may each be planar or curved.
Optionally, in the use state of the milling cutter head, the first cutting face 13 is always in a vertical state.
In an alternative of this embodiment, which is shown in fig. 3 to 6, the milling cutter head further comprises a first 16, a second 17 and a third 18 cutting surface. The first, second and third cut surfaces 16, 17 and 18 are obtained by cutting away part of the entity of the blank of the milling cutter head in order to form an avoidance space during the process of machining the milling cutter head.
The first cut surface 16 is formed by cutting off a part of the first tool surface 13, and a first avoidance space is obtained through the first cut surface 16; the second cut surface 17 is formed by cutting off a part of the second tool surface 14, and a second avoidance space is obtained through the second cut surface 17; the third cut surface 18 is formed by cutting off a part of the third rake surface 15, and a third relief space is obtained by the third cut surface 18. Wherein, the partial cutting instead of the complete cutting is to ensure that the cutting edge keeps a certain edge width, thereby ensuring the strength of the cutting edge.
When the milling cutter head rotates, a revolving body formed by revolving the straight blade 12 and the arc-shaped blades is a preset revolving body, the first cutting surface 16, the second cutting surface 17, the third cutting surface 18, the first cutter surface 13, the second cutter surface 14 and the third cutter surface 15 which form the first cutting surface 16, the second cutting surface 17 and the third cutting surface 18 are all positioned in the preset revolving body, namely, the first avoidance space, the second avoidance space and the third avoidance space play a role in avoiding the space. That is, it is ensured that the workpiece is surely milled by the contact of the cutting edge while the milling cutter head is rotated, and the first, second or third face 13, 14 or 15 is prevented from contacting the workpiece, thereby ensuring that the multi-arc-shaped solid of revolution can be milled instead of other shapes.
In an alternative of this embodiment, the first 16, second 17 and third 18 cutting surfaces are plane or curved, i.e. they can be selected according to the actual production adjustment, as long as it is possible to ensure that the cutting edges are in contact with the workpiece during the revolution, but not other parts of the milling cutter head.
In an alternative of this embodiment, the milling cutter head is formed of a diamond material. The existing milling cutter head is usually made of tungsten steel, polycrystalline diamond or cubic boron nitride, and the machining precision of the milling cutter head can not meet the requirement. And through adopting the diamond material for this milling cutter tool bit has good wear resistance, and hardness is high, makes the processing surface can reach submicron level shaping accuracy and nanometer level surface finish, and is smooth no fine line, thereby realizes whole high accuracy in the space.
Optionally, the diamond is a single crystal diamond, a natural diamond, or an artificial diamond.
In the alternative of this embodiment, the arc-shaped edge is circular-arc-shaped, so that the milling cutter head can mill a plurality of tangent arc-shaped rotators with different sizes at the same time, and the milling cutter head has wide applicability in the fields of processing high-precision optical glass lenses, electronic information and the like, and is used for performing high-light fine processing in the fields and improving the yield of the high-light fine processing.
In an alternative of this embodiment, the number of curved edges is two, i.e. only one set of first curved edge 10 and second curved edge 11 is included, so that the milling cutter head is capable of milling two tangential and differently sized circular-arc bodies of revolution simultaneously.
Example two
A second embodiment provides a milling cutter, which comprises the milling cutter head of the first embodiment, to which the features of the milling cutter head disclosed in the first embodiment are also applicable, and the features of the milling cutter head disclosed in the first embodiment will not be described again.
Fig. 1 is a schematic structural diagram of a milling cutter provided in this embodiment; FIG. 2 is an enlarged view of a portion of FIG. 1 at A; FIG. 3 is a left side view of FIG. 1; FIG. 4 is an enlarged view of a portion of FIG. 3 at B; FIG. 5 is a top view of FIG. 1; fig. 6 is a partial enlarged view of fig. 5 at C. Wherein fig. 2, 4 and 6 clearly show the specific structure of the milling cutter head in the first embodiment.
Referring to fig. 1 to 6, the present embodiment provides a milling cutter including a milling cutter head.
The advantages of the embodiment one milling cutter head are provided by the milling cutter according to the present embodiment, and the advantages of the embodiment one disclosed milling cutter head will not be described again here.
In an alternative of this embodiment, the milling cutter further includes a milling cutter holder 20, the milling cutter holder 20 includes a holder body 200 and a head base 201, and the milling cutter head is welded to the head base 201. The driving piece can control the milling cutter head to rotate or feed by controlling the rotation or feeding of the milling cutter handle 20, so that the milling function of the milling cutter is realized.
In the alternative of this embodiment, the tool bit holder 201 and the tool holder body 200 are made of tungsten steel, and tungsten steel has the characteristics of high hardness, high strength, high toughness, high vibration resistance and the like. On the one hand, in the process of processing the milling cutter head, weld the blank of milling cutter head in headstock 201 earlier and then carry out rough machining and finish machining to milling cutter head, because the runout volume of handle of a knife body 200 is minimum, can guarantee that the cutting edge of the milling cutter head who processes does not produce the breach, specifically, the precision can reach and enlarge under 3000 times and the cutting edge does not have the breach. On the other hand, because the runout of the tool holder body 200 is extremely small, when the milling cutter head is used for cutting a workpiece, the coaxiality of the machined revolving body can be improved, and a foundation is provided for machining a high-precision product by the milling cutter.
Optionally, the tool bit seat 201 and the tool shank body 200 are integrally formed.
In an alternative of this embodiment, the holder 201 is semi-cylindrical and the milling cutter head is welded to the planar side wall of the holder 201. In particular, it has to be ensured that all the arc-shaped edges and straight edges 12 of the milling cutter head are exposed to the planar side wall of the head seat 201.
Optionally, the first cutting face 13 of the milling cutter head is welded to the planar side wall of the head seat 201.
Finally, it should be noted that: the above embodiments are only used to illustrate the technical solution of the present invention, and not to limit the same; while the invention has been described in detail and with reference to the foregoing embodiments, it will be understood by those skilled in the art that: the technical solutions described in the foregoing embodiments may still be modified, or some or all of the technical features may be equivalently replaced; and the modifications or the substitutions do not make the essence of the corresponding technical solutions depart from the scope of the technical solutions of the embodiments of the present invention. Furthermore, those skilled in the art will appreciate that while some embodiments described herein include some features included in other embodiments, rather than other features, combinations of features of different embodiments are meant to be within the scope of the invention and form different embodiments. For example, any of the claimed embodiments may be used in any combination. The information disclosed in this background section is only for enhancement of understanding of the general background of the invention and should not be taken as an acknowledgement or any form of suggestion that this information forms the prior art already known to a person skilled in the art.
Claims (10)
1. The milling cutter head is characterized by comprising a plurality of arc-shaped blades which are sequentially connected end to end, wherein the arc-shaped blade positioned at the head side in two adjacent arc-shaped blades is internally tangent to the arc-shaped blade positioned at the tail side.
2. Milling cutter head according to claim 1,
the milling cutter head also comprises a straight edge which is connected with and tangent to the head ends of the plurality of arc-shaped edges;
the tangent line of the tail ends of the arc-shaped edges is perpendicular to the straight edge.
3. The milling cutter head according to claim 2, further comprising first and second angled faces, the junction of the first and second faces forming the arcuate edge.
4. The milling cutter head according to claim 3, further comprising a third face connected at an included angle to the first face, the third face and the second face both being on the same side of the first face;
the straight edge is formed at the joint of the third knife face and the first knife face.
5. The milling cutter head according to claim 4, further comprising a first, a second and a third cut-out surface;
the first cut surface is formed by cutting off a part of the first blade surface, the second cut surface is formed by cutting off a part of the second blade surface, and the third cut surface is formed by cutting off a part of the third blade surface;
when the milling cutter head rotates, the straight blade and the plurality of arc-shaped blades rotate to form a predetermined rotation body, and the first cutting surface, the second cutting surface, the third cutting surface, and the first cutter surface, the second cutter surface, and the third cutter surface which form the first cutting surface, the second cutting surface, and the third cutting surface are all located in the predetermined rotation body.
6. Milling cutter head according to claim 5,
the first, second and third cut-out surfaces are planar or curved.
7. Milling cutter head according to claim 1, characterized in that the milling cutter head is formed of a diamond material;
the arc-shaped blade is arc-shaped;
the number of the arc-shaped edges is two.
8. Milling cutter tool, characterized in that it comprises a milling cutter head according to any one of claims 1 to 7.
9. The milling cutter according to claim 8, further comprising a milling cutter shank including a shank body and a head seat, the milling cutter head being welded to the head seat.
10. The milling cutter according to claim 9, wherein the tool tip carrier and the tool shank body are both formed of tungsten steel;
and/or the cutter head seat is semi-cylindrical, and the milling cutter head is welded on the plane side wall of the cutter head seat.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010115424.8A CN111136315B (en) | 2020-02-25 | 2020-02-25 | Milling cutter head and milling cutter |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010115424.8A CN111136315B (en) | 2020-02-25 | 2020-02-25 | Milling cutter head and milling cutter |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN111136315A true CN111136315A (en) | 2020-05-12 |
| CN111136315B CN111136315B (en) | 2024-07-05 |
Family
ID=70527985
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010115424.8A Active CN111136315B (en) | 2020-02-25 | 2020-02-25 | Milling cutter head and milling cutter |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111136315B (en) |
Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| TWM297803U (en) * | 2006-04-19 | 2006-09-21 | Jia-Fen Yu | Engraving knife |
| JP2007229849A (en) * | 2006-02-28 | 2007-09-13 | Jtekt Corp | End mill and processing method using the same |
| CN101534983A (en) * | 2006-11-28 | 2009-09-16 | 钴碳化钨硬质合金公司 | Drill for making flat bottom hole |
| CN202278238U (en) * | 2011-09-14 | 2012-06-20 | 西安飞机工业(集团)有限责任公司 | Numerically-controlled arc milling cutter |
| CN104209565A (en) * | 2014-09-28 | 2014-12-17 | 江西杰浩硬质合金工具有限公司 | Three-edge profile cutter |
| CN104411430A (en) * | 2012-06-21 | 2015-03-11 | 住友电工硬质合金株式会社 | Cutting tool |
| CN104439335A (en) * | 2014-10-31 | 2015-03-25 | 常州华尔澜工具有限公司 | Novel hard alloy molding knife |
| JP2015171762A (en) * | 2015-07-06 | 2015-10-01 | 三菱マテリアル株式会社 | ball end mill |
| CN205342040U (en) * | 2016-01-13 | 2016-06-29 | 江西杰浩硬质合金工具有限公司 | Milling cutter |
| CN206253707U (en) * | 2016-12-20 | 2017-06-16 | 江西杰浩硬质合金工具有限公司 | Become spiral forming milling cutter |
| CN211915629U (en) * | 2020-02-25 | 2020-11-13 | 深圳市誉和光学精密刀具有限公司 | Milling cutter head and milling cutter |
-
2020
- 2020-02-25 CN CN202010115424.8A patent/CN111136315B/en active Active
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007229849A (en) * | 2006-02-28 | 2007-09-13 | Jtekt Corp | End mill and processing method using the same |
| TWM297803U (en) * | 2006-04-19 | 2006-09-21 | Jia-Fen Yu | Engraving knife |
| CN101534983A (en) * | 2006-11-28 | 2009-09-16 | 钴碳化钨硬质合金公司 | Drill for making flat bottom hole |
| CN202278238U (en) * | 2011-09-14 | 2012-06-20 | 西安飞机工业(集团)有限责任公司 | Numerically-controlled arc milling cutter |
| CN104411430A (en) * | 2012-06-21 | 2015-03-11 | 住友电工硬质合金株式会社 | Cutting tool |
| CN104209565A (en) * | 2014-09-28 | 2014-12-17 | 江西杰浩硬质合金工具有限公司 | Three-edge profile cutter |
| CN104439335A (en) * | 2014-10-31 | 2015-03-25 | 常州华尔澜工具有限公司 | Novel hard alloy molding knife |
| JP2015171762A (en) * | 2015-07-06 | 2015-10-01 | 三菱マテリアル株式会社 | ball end mill |
| CN205342040U (en) * | 2016-01-13 | 2016-06-29 | 江西杰浩硬质合金工具有限公司 | Milling cutter |
| CN206253707U (en) * | 2016-12-20 | 2017-06-16 | 江西杰浩硬质合金工具有限公司 | Become spiral forming milling cutter |
| CN211915629U (en) * | 2020-02-25 | 2020-11-13 | 深圳市誉和光学精密刀具有限公司 | Milling cutter head and milling cutter |
Also Published As
| Publication number | Publication date |
|---|---|
| CN111136315B (en) | 2024-07-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5744235B2 (en) | Radius end mill | |
| US7908945B2 (en) | Antirotation tool holder and cutting insert | |
| CN103842118A (en) | Cutting insert and exchangeable-blade cutting tool | |
| JP4860882B2 (en) | Milling tools | |
| TW201008681A (en) | Milling cutter and cutting insert therefor | |
| CN108290231B (en) | Indexable insert blade type rotary cutting tool and blade | |
| US6890134B1 (en) | Method of producing endodontic instruments | |
| CN111822765B (en) | Cutting insert | |
| US4060881A (en) | Cutter head assembly for gear cutting machines | |
| CN211915629U (en) | Milling cutter head and milling cutter | |
| US20210008635A1 (en) | Turning tool and turning method for cnc-machines | |
| JP4796678B2 (en) | Tip flank grinding forming method and rotary cutting tool | |
| JP2010179409A (en) | Cutting tool | |
| JP5312538B2 (en) | Throwaway end mill | |
| CN111421173B (en) | Green body and cutting tool with spiral superhard material rake face | |
| CN111136315B (en) | Milling cutter head and milling cutter | |
| JPH07506059A (en) | How to adjust and angle the cutter blade by sharpening it | |
| JP4048685B2 (en) | Throwaway tip | |
| CN111482689B (en) | Cutter of welding gun cap sharpening machine | |
| JP2019093497A (en) | Cutting insert and blade edge replaceable type rotary cutting tool | |
| JP2010149231A (en) | Cutting tool and method of polishing the same | |
| JP2010058240A (en) | Edge replacement type cutting tool | |
| CN114260513B (en) | Cutter preparation method and cutter | |
| CN220515531U (en) | Dovetail reverse taper staggered blade milling cutter | |
| JPS5841060Y2 (en) | Throwaway tip |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |