CN111022582A - Large-contact-surface low-stress chain, braided core and preparation method - Google Patents
Large-contact-surface low-stress chain, braided core and preparation method Download PDFInfo
- Publication number
- CN111022582A CN111022582A CN201911376329.7A CN201911376329A CN111022582A CN 111022582 A CN111022582 A CN 111022582A CN 201911376329 A CN201911376329 A CN 201911376329A CN 111022582 A CN111022582 A CN 111022582A
- Authority
- CN
- China
- Prior art keywords
- chain
- contact
- radius
- section
- ring
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images



Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16G—BELTS, CABLES, OR ROPES, PREDOMINANTLY USED FOR DRIVING PURPOSES; CHAINS; FITTINGS PREDOMINANTLY USED THEREFOR
- F16G15/00—Chain couplings, Shackles; Chain joints; Chain links; Chain bushes
- F16G15/12—Chain links
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21L—MAKING METAL CHAINS
- B21L1/00—Making chains or chain links by bending workpieces of rod, wire, or strip to form links of oval or other simple shape
- B21L1/02—Making chains or chain links by bending workpieces of rod, wire, or strip to form links of oval or other simple shape by bending the ends of the workpieces to abut
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Wire Processing (AREA)
Abstract
The invention relates to a large-contact-surface low-stress chain, a braided core and a preparation method, and belongs to the technical field of mining chains. The invention designs a new radius of the outer edge profile of the braided core circular arc section, so that the cross section of the circular arc section of the chain link is changed into a chain link formed by a plurality of circular arcs in the process of bending a bar into the chain link, the radius of the cross section of one side, which is in contact with the adjacent chain link, is equal to or approximately equal to the radius of the circular arc at the inner side of the adjacent chain link, the contact surfaces of the two adjacent chain links are in contact in a concentric circle mode, and the whole contact surface is approximately a saddle surface, thereby realizing a novel chain link contact form, increasing the contact area between the adjacent chain links, reducing the contact stress of the contact area of the chain links, reducing the risks of contact fatigue, corrosion fatigue and stress corrosion of the chain links, and prolonging.
Description
Technical Field
The invention belongs to the technical field of mining chains, and particularly relates to a large-contact-surface low-stress chain, a braided core and a preparation method.
Background
Currently, there are two main types of mining chains, one type is a round-link chain, all chain links are circular section bars and are bent into rings, and then welding forming, the other type is compact chain and super flat chain, and is formed by connecting round rings and flat rings in turn, the round rings are usually circular section bars and are welded and formed after bending along a braided core, the flat rings are usually integrally forged and formed, or flat bars with different section shapes are forged by round bars and are then welded and formed along the braided core. The circular arc sections of the connecting portions of two adjacent links are circular or semicircular in cross-section, as shown in the shape of the hatched portion in fig. 1, for any type of chain currently used. In general, when the bar stock is bent and formed along the braided core, the outer dimension of the braided core at the circular arc section is designed to be the same as or similar to the diameter of the bar stock so as to restrain the bar stock to keep the shape of the circular section as much as possible during the bending deformation. As the circular section of the circular arc section of the chain ring of the bar stock is slightly deformed in the bending deformation process, the diameter along the length direction of the chain is slightly smaller, and the diameter of the section is slightly increased in the direction perpendicular to the length direction of the chain, so that the diameter of the section has the condition of a long axis and a short axis, but the overall section is still circular, and the radius of the circular arc is still approximately equal to the diameter of the bar stock.
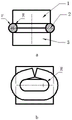
FIG. 1 is a schematic view of a typical link bending of a prior art chain. In fig. 1, 1 is an upper end die of a braided core, 2 is a cross section profile of a bent chain ring, and 3 is a lower end die of the braided core. Typically the radius r of the die is equal or approximately equal to the radius of the link bar stock. For ease of understanding, the 3 radii and symbols involved need to be described here. First is the cross-sectional radius of the bar, denoted by r. Secondly, when the bar stock is bent into a chain ring, the axis of the bar stock can be bent and deformed along the braided core with two circular arcs at two ends, and when the top view of the figure 1 is seen, the bar stock can have contour lines of two circular arcs at the circular arc section after being bent and deformed, wherein the radius of the bending circular arc of the bar stock coincident with the braided core circular arc is R. Finally, the surface of the braided core contacted with the bar is not formed by curling a plane along the outer contour line of the braided core, but is a groove-shaped curved surface formed by sweeping a semi-circular curve with the radius approximately equal to the section radius r of the bar along the outer contour line of the braided core, the bending process of the bar is actually embedded in the U-shaped groove of the braided core to deform, the radius of the bottom of the groove is usually (1-1.05) r, the cross section of the circular arc section of the bar after bending deformation is still approximately circular with the radius r due to the constraint effect of the braided core groove, and the section radius of the braided core U-shaped groove is (1-1.05) r and is consistent with the section radius of the bar.
In the existing chain ring, the circular arc sections contacted at the connecting parts of the two chain rings are all circular, as shown in fig. 2, in the figure, R is the inner circular arc radius of the circular arc section of the chain ring, and R is the section radius of the circular arc sections of the flat ring and the vertical ring. In fig. 2, the contact between the vertical ring and the flat ring is actually the contact in a way that the circular arc with the radius R of the vertical ring is tangent to the circular arc with the radius R of the flat ring, the contact surface is actually a point, and the actual contact surface is a relatively small cross shape due to deformation of the chain ring in the process of tensile force. The link contact location can develop a large compressive stress, the existence of the stress can cause the contact location to wear quickly, contact fatigue is easy to occur, tensile stress can be further formed inside the crack after the crack occurs, and stress corrosion can be caused in a corrosive environment, so that the failure and the fracture of the chain are accelerated.
Disclosure of Invention
Technical problem to be solved
The technical problem to be solved by the invention is as follows: how to prolong the service life of the chain.
(II) technical scheme
In order to solve the technical problem, the invention provides a method for designing a braided core of a large-contact-surface low-stress chain, wherein the radius of a U-shaped groove in contact with an arc section of a rod material of a chain link is designed to be 0.85-1.15 times of the radius R of an inner arc of the arc section of the chain link.
Preferably, the radius of the U-shaped groove of the braided core contacting the circular arc section of the chain link rod material is designed to be the inner circular arc radius R of the circular arc section of the chain link.
The invention also provides a braided core designed by the design method.
The invention also provides a preparation method of the large-contact-surface low-stress chain, in the method, the chain ring of the chain is made of a chain ring bar material, and the braided core is used for bending and forming.
Preferably, the link bar stock used is round bar stock.
The invention also provides a large-contact-surface low-stress chain prepared by the preparation method.
Preferably, in the chain ring of the chain, the section of the circular arc section of the vertical ring in contact with the flat ring comprises a plurality of circular arcs, wherein the radius of the side surface in contact with the flat ring is (0.85-1.15) R, and the radius of the non-contact side is the original radius R of the bar stock of the chain ring; the section of the circular arc section of the flat ring in contact with the vertical ring also comprises a plurality of sections of circular arcs, wherein the radius of the side surface in contact with the vertical ring is (0.85-1.15) R, and the radius of the non-contact side is R.
Preferably, in the chain links of the chain, the section of the circular arc section of the vertical ring in contact with the flat ring comprises two circular arcs, wherein the radius of the side surface in contact with the flat ring is R, and the radius of the non-contact side is the original radius R of the bar material of the chain link; the section of the circular arc section of the flat ring in contact with the vertical ring also comprises two circular arcs, wherein the radius of the side surface in contact with the vertical ring is R, and the radius of the non-contact side is R.
Preferably, the chain is a mining chain.
(III) advantageous effects
The invention designs a new radius of the outer edge profile of the braided core circular arc section, so that the cross section of the circular arc section of the chain link is changed into a chain link formed by a plurality of circular arcs in the process of bending a bar into the chain link, the radius of the cross section of one side, which is in contact with the adjacent chain link, is equal to or approximately equal to the radius of the circular arc at the inner side of the adjacent chain link, the contact surfaces of the two adjacent chain links are in contact in a concentric circle mode, and the whole contact surface is approximately a saddle surface, thereby realizing a novel chain link contact form, increasing the contact area between the adjacent chain links, reducing the contact stress of the contact area of the chain links, reducing the risks of contact fatigue, corrosion fatigue and stress corrosion of the chain links, and prolonging.
Drawings
FIG. 1 is a schematic view of a typical link bend forming;
FIG. 2 is a schematic view of the cross-sectional shape of the circular arc apex of a conventional chain link;
FIG. 3 is a schematic view of the bending of a chain link according to the present invention;
FIG. 4 is a sectional view of the chain ring circular arc segment of the present invention.
Detailed Description
In order to make the objects, contents, and advantages of the present invention clearer, the following detailed description of the embodiments of the present invention will be made in conjunction with the accompanying drawings and examples.
When the links are made of round bar stock, they must be bent by means of a braiding core. The invention designs a novel braided core, wherein the radius of a U-shaped groove in contact with the circular arc section of a bar material is designed into the radius R or the approximate value R of the circular arc in the circular arc section of a chain ring. Specifically, as shown in fig. 3, 1 is the upper end mold of the braid core, 2 is the curved link cross-sectional profile, and 3 is the lower end mold of the braid core. When the bar is bent and formed along the braided core of the structure, the section shape of the bar can be deformed into 0.85-1.15 times of the bending profile radius R of the braided core due to the extrusion action on the side of the circular arc section of the chain ring, which is contacted with the braided core. The cross section of the circular arc section of the chain ring formed by the core braiding can be deformed into a shape that the radius of the side far away from the core braiding is the initial radius R of the bar, and the radius of the side close to the core braiding is 0.85-1.15 times of the bending profile radius R of the core braiding.
FIG. 4 is a schematic view of a welded link formed by bending the link according to the present invention. In FIG. 4, the joints of the flat ring and the vertical ring are all multi-segment circular arcs. Namely, the section of the circular arc section of the vertical ring in contact with the flat ring is mainly composed of a plurality of circular arcs, the radius of the side face in contact with the flat ring is (0.85-1.15) R, the radius of the non-contact side is R, the section of the circular arc section of the flat ring is also the same, the radius of the side face in contact with the vertical ring is (0.85-1.15) R, the radius of the non-contact side is R, and R is the original radius of a chain ring bar, and the section radius of the side face of the circular arc section in contact with an adjacent chain ring is numerically equal to (0.85-1.15) R due to extrusion deformation of the bar along the outer edge profile of the braided core in the bending process. Therefore, on the contact surface of the flat ring and the vertical ring, the radius of the arc section on the inner side of the flat ring is approximately equal to the radius of the section of the vertical ring bar, and the multiple sections of arc surfaces are contacted in a concentric circle mode, so that the contact area is greatly increased, the contact stress is reduced, and the possibility of fatigue cracking and stress corrosion cracking is reduced.
The above description is only a preferred embodiment of the present invention, and it should be noted that, for those skilled in the art, several modifications and variations can be made without departing from the technical principle of the present invention, and these modifications and variations should also be regarded as the protection scope of the present invention.
Claims (9)
1. A design method for a braided core of a chain with a large contact surface and low stress is characterized in that the radius of a U-shaped groove in contact with an arc section of a rod material of a chain link of the braided core is designed to be 0.85-1.15 times of the radius R of an inner arc of the arc section of the chain link.
2. The method of claim 1 wherein the radius of the U-shaped groove where the braid contacts the circular segment of the rod material of the chain link is designed to be the radius R of the circular segment of the chain link.
3. A braid core designed by the design method of claim 1 or 2.
4. A method of manufacturing a large contact surface low stress chain, wherein the links of the chain are made from a rod of links and are bent using a braid core according to claim 3.
5. The method of claim 4, wherein the rod of the link used is a round rod.
6. A large contact area low stress chain produced by the production method according to claim 4 or 5.
7. The large contact surface low stress chain as claimed in claim 6, wherein the section of the circular arc section of the vertical ring contacting the flat ring in the chain ring of the chain comprises a plurality of circular arcs, wherein the radius of the side contacting the flat ring is (0.85-1.15) R, and the radius of the non-contact side is the original radius R of the bar stock of the chain ring; the section of the circular arc section of the flat ring in contact with the vertical ring also comprises a plurality of sections of circular arcs, wherein the radius of the side surface in contact with the vertical ring is (0.85-1.15) R, and the radius of the non-contact side is R.
8. The large contact surface low stress chain as claimed in claim 6, wherein the section of the circular arc section of the vertical ring contacting the flat ring in the chain link comprises two circular arcs, wherein the radius of the side contacting the flat ring is R, and the radius of the non-contact side is the original radius R of the link bar; the section of the circular arc section of the flat ring in contact with the vertical ring also comprises two circular arcs, wherein the radius of the side surface in contact with the vertical ring is R, and the radius of the non-contact side is R.
9. A large contact surface low stress chain according to claim 6 or 7 or 8, wherein said chain is a mining chain.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911376329.7A CN111022582A (en) | 2019-12-27 | 2019-12-27 | Large-contact-surface low-stress chain, braided core and preparation method |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911376329.7A CN111022582A (en) | 2019-12-27 | 2019-12-27 | Large-contact-surface low-stress chain, braided core and preparation method |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111022582A true CN111022582A (en) | 2020-04-17 |
Family
ID=70194505
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201911376329.7A Pending CN111022582A (en) | 2019-12-27 | 2019-12-27 | Large-contact-surface low-stress chain, braided core and preparation method |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111022582A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116689696A (en) * | 2023-06-25 | 2023-09-05 | 宁夏天地奔牛链条有限公司 | Mining equal-strength compact chain and manufacturing method thereof |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3744239A (en) * | 1971-12-20 | 1973-07-10 | T Anson | Chain link with extended wear surface |
| US3864906A (en) * | 1973-06-22 | 1975-02-11 | Vickers Ruwolt Pty Ltd | Chain link |
| JPS554884U (en) * | 1979-06-13 | 1980-01-12 | ||
| CN103534512A (en) * | 2011-05-17 | 2014-01-22 | 蒂勒有限及两合公司 | Round steel chain |
| RU2561545C1 (en) * | 2014-04-01 | 2015-08-27 | Виктор Евгеньевич Серебряков | Chain for chain curtain of roasting unit |
| CN212055681U (en) * | 2019-12-27 | 2020-12-01 | 北京华海基业机械设备有限公司 | Large contact surface low stress chain and braided core |
-
2019
- 2019-12-27 CN CN201911376329.7A patent/CN111022582A/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3744239A (en) * | 1971-12-20 | 1973-07-10 | T Anson | Chain link with extended wear surface |
| US3864906A (en) * | 1973-06-22 | 1975-02-11 | Vickers Ruwolt Pty Ltd | Chain link |
| JPS554884U (en) * | 1979-06-13 | 1980-01-12 | ||
| CN103534512A (en) * | 2011-05-17 | 2014-01-22 | 蒂勒有限及两合公司 | Round steel chain |
| RU2561545C1 (en) * | 2014-04-01 | 2015-08-27 | Виктор Евгеньевич Серебряков | Chain for chain curtain of roasting unit |
| CN212055681U (en) * | 2019-12-27 | 2020-12-01 | 北京华海基业机械设备有限公司 | Large contact surface low stress chain and braided core |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116689696A (en) * | 2023-06-25 | 2023-09-05 | 宁夏天地奔牛链条有限公司 | Mining equal-strength compact chain and manufacturing method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN212055681U (en) | Large contact surface low stress chain and braided core | |
| CN201125343Y (en) | Surface contact structure cable wire | |
| US8793969B2 (en) | Round steel chain | |
| CN105526449A (en) | Two-part or multi-part double-layer type wearproof impact-resistant tube and manufacture method thereof | |
| EP1728018B9 (en) | Threaded tubular connection which is resistant to bending stresses | |
| KR101446047B1 (en) | Pipe connection | |
| US5946898A (en) | Wire rope having an independent wire rope core | |
| KR101171118B1 (en) | Expanded graphite-made knitting yarn and the gland packing | |
| CN101581048B (en) | Stainless steel wire for spaceflight | |
| CN103998820B (en) | Chain link chain link | |
| CN101218451B (en) | Link chain and method for producing a link chain | |
| CN113550995B (en) | Design method for spacer bush of rod end spherical hinge | |
| CN101360962B (en) | Flexible liquid pipe and method of manufacturing the same | |
| EA007264B1 (en) | A flexible, tubular device e.g. a bellows | |
| CN115231200A (en) | A high-strength forged flat-ring compact chain for conveying equipment | |
| CN109563732B (en) | Threaded joints for oil and gas pipelines | |
| EP3098496B1 (en) | Threaded joint for pipe | |
| EP2807400B1 (en) | Chinese finger with flat or flattened filaments | |
| CN203258282U (en) | Double-layer expansion joint | |
| CN203729934U (en) | Expansion cone | |
| CN111842775A (en) | A wear-resistant variable-pitch chain and its processing technology | |
| WO2021033497A1 (en) | Wire rope | |
| CN219198009U (en) | Reducing chain link and reducing chain | |
| CN201447620U (en) | Nine-strand steel wire rope | |
| CN207634823U (en) | A kind of bellows |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200417 |