CN110879031A - Detection mechanism and detection method for inner side sinking platform surface of part - Google Patents
Detection mechanism and detection method for inner side sinking platform surface of part Download PDFInfo
- Publication number
- CN110879031A CN110879031A CN201911217199.2A CN201911217199A CN110879031A CN 110879031 A CN110879031 A CN 110879031A CN 201911217199 A CN201911217199 A CN 201911217199A CN 110879031 A CN110879031 A CN 110879031A
- Authority
- CN
- China
- Prior art keywords
- detection
- detected
- pin
- sinking
- sinking platform
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B5/00—Measuring arrangements characterised by the use of mechanical techniques
- G01B5/18—Measuring arrangements characterised by the use of mechanical techniques for measuring depth
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B5/00—Measuring arrangements characterised by the use of mechanical techniques
- G01B5/0002—Arrangements for supporting, fixing or guiding the measuring instrument or the object to be measured
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B5/00—Measuring arrangements characterised by the use of mechanical techniques
- G01B5/14—Measuring arrangements characterised by the use of mechanical techniques for measuring distance or clearance between spaced objects or spaced apertures
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- A Measuring Device Byusing Mechanical Method (AREA)
Abstract
The invention discloses a detection mechanism and a detection method for an inner side sinking platform surface of a part, and relates to the technical field of detection tools. The detection mechanism for the sunken table surface on the inner side of the part comprises a base, a detection support and a detection pin, wherein the base is provided with a detection table surface for placing the part to be detected; the detection support is arranged on the base and comprises a mounting frame positioned above the detection table top, a mounting hole is formed in the mounting frame, and a first detection surface is formed on the upper surface of the mounting frame; the detection pin is movably arranged in the mounting hole in the vertical direction, and a second detection surface is formed on the detection pin. According to the invention, when the part to be detected is placed on the detection table surface, the detection pin is moved downwards until the lower end of the detection pin contacts the bottom of the sinking table surface of the part to be detected, and the depth or the depth deviation of the sinking table surface is measured according to the displacement change of the second detection surface relative to the first detection surface, so that the measurement precision of the sinking table surface of the part is improved.
Description
Technical Field
The invention relates to the technical field of detection tools, in particular to a mechanism and a method for detecting an inner side sinking platform surface of a part.
Background
The checking fixture is special checking equipment for measuring and evaluating the size and quality of parts. When the part is accurately fixed on the checking fixture, the hole site, the molded surface and the periphery of the part are checked by visual inspection or by means of checking tools such as a measuring meter, a caliper and a checking pin, and the geometric parameters of the part can be reasonably measured. The shapes of parts are various, and the detection of the sunken table surface at the inner side of the part is always a problem that an inspector is very headache.
In the prior art, the clamping plate is usually used for detecting when the depth deviation of the inner side sinking table surface of a part is measured, and the detection consistency cannot be ensured because the surface is lower and the measuring tool is difficult to use and inaccurate in reading. When the measurement requirement is high and the sinking platform surface is small, the detection cannot be carried out.
Disclosure of Invention
The invention mainly aims to provide a part inner side sinking platform surface detection mechanism and a detection method thereof, and aims to solve the problem that the part inner side sinking platform surface is difficult to detect.
In order to achieve the above object, the present invention provides a detection mechanism for an inner side sinking platform surface of a part, the detection mechanism for the inner side sinking platform surface of the part comprising:
the detection device comprises a base, a detection device and a detection device, wherein the base is provided with a detection table top for placing a part to be detected;
the detection support is arranged on the base and comprises an installation plate positioned above the detection table top, an installation hole is formed in the installation plate, and a first detection surface is formed on the upper surface of the installation plate; and the number of the first and second groups,
the detection pin is movably arranged in the mounting hole in the vertical direction, a second detection surface is formed on the detection pin, and the detection pin is used for moving downwards to the position where the lower end of the detection pin contacts the bottom of a sinking table surface of the part to be detected when the part to be detected is placed on the detection table surface, so that the depth deviation of the sinking table surface is measured according to the displacement change of the second detection surface relative to the first detection surface.
Optionally, an annular boss is arranged on the periphery of the detection pin, and the annular boss is located above the mounting plate to form a second detection surface facing the mounting plate.
Optionally, the detection pin is provided with a plurality of pins, and the mounting plate is correspondingly provided with a plurality of mounting holes.
Optionally, the detection support is rotatably mounted on the base, so that the mounting plate has a detection position above the detection table top and an avoidance position for avoiding the detection table top.
Optionally, the detection stent further comprises:
the supporting seat is fixedly arranged on the base;
and one end of the rotating arm is rotatably arranged on the supporting seat along the vertical direction, and the mounting plate is arranged at the other end of the rotating arm.
Optionally, a limiting part for clamping the rotating arm is arranged on the supporting seat;
the detection support further comprises a locking piece for limiting the rotating arm to move up and down when the rotating arm rotates to be connected with the limiting portion in a clamping mode.
Optionally, a position of the support seat connected to the rotating arm is provided with a limiting plate for limiting the size of the vertical rotating angle of the rotating arm.
Optionally, the base is provided with a positioning pin for matching with a positioning hole on the part to be detected, so as to fix the part to be detected on the detection table top.
The invention also provides a method for detecting the sinking table surface on the inner side surface of the part, which comprises the following steps:
when the part to be detected is placed on the detection table board and the detection pin moves downwards until the lower end of the detection pin contacts the bottom of the sinking table board of the part to be detected, measuring the distance S between the first detection surface and the second detection surface2;
According to the distance S2And said theoretical clearance value S1Calculating the depth deviation of the sinking platform surface of the part to be detected;
the part inner side surface sinking table surface detection method is carried out by using a part inner side surface sinking table surface detection mechanism, and the part inner side surface sinking table surface detection mechanism comprises:
the detection device comprises a base, a detection device and a detection device, wherein the base is provided with a detection table top for placing a part to be detected;
the detection support is arranged on the base and comprises an installation plate positioned above the detection table top, an installation hole is formed in the installation plate, and a first detection surface is formed on the upper surface of the installation plate; and the number of the first and second groups,
the detection pin is movably arranged in the mounting hole in the vertical direction, a second detection surface is formed on the detection pin, and the detection pin is used for moving downwards when the part to be detected is placed on the detection table surface until the lower end of the detection pin contacts the bottom of a sinking table surface of the part to be detected, so that the depth or depth deviation of the sinking table surface is measured according to the displacement change of the second detection surface relative to the first detection surface; wherein the theoretical distance from the sinking platform surface of the part to be detected to the lower surface of the mounting plate is H0The thickness of the mounting plate is H1A theoretical clearance value S is arranged between the first detection surface and the second detection surface1The second detection surface has a preset length S from the lower end of the detection pin, and S is H0+H1+S1。
Optionally, when the part to be detected is placed on the detection table top and the detection pin moves downwards until the lower end of the detection pin contacts the bottom of the sinking table top of the part to be detected, the distance S between the first detection surface and the second detection surface is measured2The measuring tool used for measuring comprises one or more of a vernier caliper, a plug piece and a clearance gauge.
According to the technical scheme, when the part to be detected is placed on the detection table surface, the detection pin is moved downwards until the lower end of the detection pin contacts the bottom of the sinking table surface of the part to be detected, and the depth deviation of the sinking table surface is measured according to the displacement change of the second detection surface relative to the first detection surface. The sinking table top for detecting the parts by using the mechanism is convenient to operate and high in measurement precision.
Drawings
In order to more clearly illustrate the embodiments of the present invention or the technical solutions in the prior art, the drawings used in the description of the embodiments or the prior art will be briefly described below, it is obvious that the drawings in the following description are only some embodiments of the present invention, and for those skilled in the art, other drawings can be obtained according to the structures shown in the drawings without creative efforts.
Fig. 1 is a schematic perspective view of an embodiment of a detection mechanism for detecting a sinking platform surface on an inner side surface of a part according to the present invention;
FIG. 2 is a side view of the part inner side sinking platform detection mechanism provided in FIG. 1;
FIG. 3 is an enlarged view of a portion of FIG. 1 at A;
fig. 4 is a schematic flow chart of an embodiment of the detection mechanism for detecting the sinking platform surface on the inner side surface of the part according to the present invention.
The reference numbers illustrate:

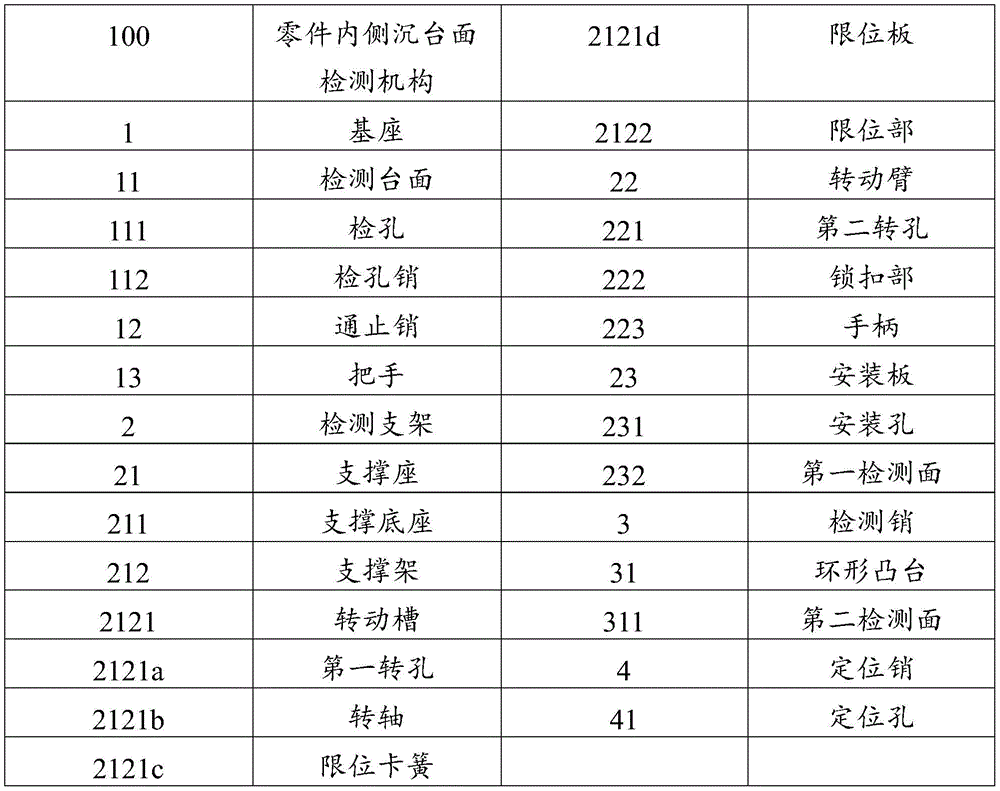
the implementation, functional features and advantages of the objects of the present invention will be further explained with reference to the accompanying drawings.
Detailed Description
The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only a part of the embodiments of the present invention, and not all of the embodiments. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
It should be noted that, if directional indications (such as up, down, left, right, front, and back … …) are involved in the embodiment of the present invention, the directional indications are only used to explain the relative positional relationship between the components, the movement situation, and the like in a specific posture (as shown in the drawing), and if the specific posture is changed, the directional indications are changed accordingly.
In addition, if there is a description of "first", "second", etc. in an embodiment of the present invention, the description of "first", "second", etc. is for descriptive purposes only and is not to be construed as indicating or implying relative importance or implicitly indicating the number of technical features indicated. Thus, a feature defined as "first" or "second" may explicitly or implicitly include at least one such feature. In addition, the meaning of "and/or" appearing throughout includes three juxtapositions, exemplified by "A and/or B" including either A or B or both A and B. In addition, technical solutions between various embodiments may be combined with each other, but must be realized by a person skilled in the art, and when the technical solutions are contradictory or cannot be realized, such a combination should not be considered to exist, and is not within the protection scope of the present invention.
The checking fixture is special checking equipment for measuring and evaluating the size and quality of parts. When the part is accurately fixed on the checking fixture, the hole site, the molded surface and the periphery of the part are checked by visual inspection or by means of checking tools such as a measuring meter, a caliper and a checking pin, and the geometric parameters of the part can be reasonably measured. The shapes of parts are various, and the detection of the sunken table surface at the inner side of the part is always a problem that an inspector is very headache. In the prior art, the sunken table surface on the inner side of the part is detected by using the clamping plate, and the measuring tool is difficult to use due to a lower surface, inaccurate in reading, incapable of guaranteeing the detection consistency and incapable of detecting when the measuring requirement is very high and the sunken table surface is smaller. In view of this, the invention provides a detection mechanism for an inner side sinking platform surface of a part, which provides convenience for measurement of the inner side sinking platform surface of the part and has a more accurate detection result.
The invention provides a detection mechanism 100 for an inner side sunken table surface of a part, and fig. 1 to 3 show an embodiment of the detection mechanism 100 for the inner side sunken table surface of the part provided by the invention, please refer to fig. 1 to 3, wherein the detection mechanism 100 for the inner side sunken table surface of the part comprises a base 1, a detection bracket 2 and a detection pin 3, and the base 1 is provided with a detection table surface 11 for placing the part to be detected; the detection support 2 is mounted on the base 1, the detection support 2 comprises a mounting plate 23 positioned above the detection table top 11, a mounting hole 231 is formed in the mounting plate 23, and a first detection surface 232 is formed on the upper surface of the mounting plate; the detection pin 3 is movably arranged in the mounting hole 231 in the vertical direction, a second detection surface 311 is formed on the detection pin 3, and the detection pin 3 is used for moving downwards until the lower end of the detection pin 3 contacts the bottom of a sinking table surface of the part to be detected when the part to be detected is placed on the detection table surface 11, so that the depth or the depth deviation of the sinking table surface can be measured according to the displacement change of the second detection surface 311 relative to the first detection surface 232.
In the technical scheme of the invention, when the part to be detected is placed on the detection table 11, the detection pin 3 is moved downwards until the lower end of the detection pin 3 contacts the bottom of the sinking table of the part to be detected, and the depth or the depth deviation of the sinking table is measured according to the displacement change of the second detection surface 311 relative to the first detection surface 232. The sinking table top for detecting the parts by using the mechanism is convenient to operate and high in measurement precision.
Specifically, referring to fig. 2, a horizontal plane is disposed on the base 1, the detection table 11 and the detection bracket 2 are both fixedly mounted on the horizontal plane, the mounting plate 23 is fixedly mounted on the detection bracket 2, and the first detection surface 232 on the upper surface of the mounting plate 23 is horizontally disposed. Preferably, a handle 13 and a through-stop pin 12 are arranged on the base 1, the handle 13 is used for moving the part inner side sinking platform surface detection mechanism 100 so as to facilitate hoisting operation, and the through-stop pin 12 can be used for roughly detecting a small hole of a part; the detection table top 11 is also provided with a hole inspection 111 and a hole inspection pin 112 for detecting the large hole of the part.
Further, referring to fig. 1, the detecting pin 3 is rod-shaped, and an annular boss 31 is disposed on the rod, and the annular boss 31 is located above the mounting plate 23 to form a second detecting surface 311 disposed toward the mounting plate 23. Preferably, the portions from the detecting pin 3 to the annular boss 31 to the lower end of the detecting pin 3 are vertically movably disposed in the mounting hole 231, and the second detecting surface 311 is always in a horizontal state during the movement. So as to be more accurate when measuring the displacement change of the second detection surface 311 with respect to the first detection surface 232. It should be noted that the detection pin 3 can be taken out from the mounting hole 231, and the length of the detection pin 3 to the portion from the annular boss 31 to the lower end of the detection pin 3 can be designed according to the parts.
Furthermore, the detecting pin 3 is provided with a plurality of detecting pins, and the mounting plate 23 is correspondingly provided with a plurality of mounting holes 231, so as to detect the sinking platform surfaces of a plurality of parts at the same time.
Referring to fig. 1, the detecting bracket 2 is rotatably mounted on the base 1, so that the mounting plate 23 has a detecting position above the detecting table 11 and an avoiding position for avoiding the detecting table 11. So that the component is placed on the inspection table 11.
Specifically, the detection bracket 2 further comprises a support base 21 and a rotating arm 22, wherein the support base 21 is fixedly mounted on the base 1. Preferably, the supporting base 21 includes a supporting base 211 and a supporting frame 212, the supporting base 211 is fixed on the base 1 by bolts for easy replacement, and the position of the horizontal plane where the first detecting surface 232 is located can be changed by arranging different supporting bases 211. The support frame 212 passes through the bolt fastening and is in on the support base 211, be equipped with on the support frame 212 and be located left rotation groove 2121 and be located the fixed slot on right side, be equipped with first commentaries on classics hole 2121a on the cell wall of rotation groove 2121, the left end of rotor arm 22 has the second of coaxial setting and changes hole 221, the support frame 212 still is equipped with pivot 2121b, pivot 2121b wear to establish with first commentaries on classics hole 2121a with second commentaries on classics hole 221 and both ends are revealed, mounting panel 23 install in the right-hand member of rotor arm 22, so that the rotor arm 22 drives mounting panel 23 winds pivot 2121b tilting. The mounting plate 23 is fixed to the right end of the pivot arm 22 by a bolt. Preferably, the exposed portion of the rotating shaft 2121b is fixed by a limit clamp spring 2121c to prevent the rotating shaft 2121b from falling off from the first rotating hole 2121a and the second rotating hole 221.
Furthermore, a limiting part 2122 for clamping the rotating arm 22 is arranged on the supporting seat 21; the detecting bracket 2 further includes a locking portion 222 for limiting the up-and-down movement of the rotating arm 22 when the rotating arm 22 rotates to be clamped with the limiting portion 2122. Preferably, the limiting portion 2122 is disposed on the supporting frame 212 of the supporting seat 21 and located at the right side of the supporting frame 212, the limiting portion 2122 is a groove with a screw hole, the locking portion 222 is disposed on the rotating arm 22, and the locking portion 222 is a knob with a bolt. When the part to be detected is replaced, the rotating arm 22 is rotated to the limiting part 2122, so that the detection support 2 is located in the working state again, and the knob is screwed and the bolt is driven to fix the rotating arm 22, so that the effect of fixing the mounting plate 23 is achieved.
Preferably, a position of the support seat 21 connected to the rotating arm 22 is provided with a limit plate 2121d for limiting the size of the vertical rotating angle of the rotating arm 22. A handle 223 is provided on the rotating arm 22 to facilitate rotation of the rotating arm 22.
Preferably, the part inner side surface sinking platform surface detection 100 further includes a positioning pin 4 (not shown in the figure) for matching with the positioning hole 41 on the part to be detected, so as to fix the part to be detected on the detection platform surface 11. Here, the parts to be inspected are generally provided with positioning holes for positioning.
The invention also provides a method for detecting the sinking table surface on the inner side surface of the part, which is carried out by using the mechanism 100 for detecting the sinking table surface on the inner side surface of the part. Referring to fig. 3 and 4, the theoretical distance from the countertop of the part to the lower end of the mounting plate is H0The thickness of the mounting plate is H1A theoretical gap value S is set between the first detection surface 232 and the second detection surface 3111The second detecting surface 311 and the lower end of the detecting pin 3 have a preset length S, and S is equal to H0+H1+S1。
It should be noted that the theoretical distance H from the sinking platform surface of the part to the lower end of the mounting plate0The sum of the theoretical depth of the part sinking platform surface and the distance from the part non-sinking platform surface to the lower surface of the mounting plate 23; the preset length S is obtained by comprehensively calculating the theoretical depth of the sinking platform surface of the part and the height of the mounting plate 23 from the part; the detection pin 3 is designed according to different parts, the lower end of the detection pin is provided with an end face following the shape of the sinking table surface of the part 5 to be detected, and the detection table surface 11 can also be designed following the shape of the part; setting the theoretical clearance value S1Measurement and calculation can be facilitated. The method for detecting the sunken table surface on the inner side surface of the part comprises the following steps:
step S10, when the part 5 to be detected is placed on the detection table 11 and the detection pin 3 moves downward until the lower end of the detection pin 3 contacts the bottom of the sinking table of the part 5 to be detected, measuring the distance S between the first detection surface 232 and the second detection surface 3112。
In the present embodiment, the distance S between the first detection surface 232 and the second detection surface 311 is measured2In this case, the measuring tool includes one or more of a vernier caliper, a plug and a clearance gauge.
In specific implementation, the part 5 to be detected is placed on the detection table top 11; inserting the positioning pin 4 into the positioning hole 41 to fix the part 5 to be detected; then through the handles 223 andthe locking part 222 makes the detecting bracket 2 in a stable working state; finally, the detection pin 3 is inserted into the mounting hole 231 until the lower end of the detection pin 3 contacts the bottom of the sinking platform of the part 5 to be detected, and the distance S between the first detection surface 232 and the second detection surface 311 is measured2。
Step S20, according to the distance S2And said theoretical clearance value S1And calculating the depth deviation of the sinking platform surface of the part to be detected 5.
In the present embodiment, the theoretical gap value S between the first detection surface 232 and the second detection surface 31113mm, the depth deviation value of the sinking platform surface of the part to be detected 5 is +/-S2-3mm)。
The above description is only a preferred embodiment of the present invention, and is not intended to limit the scope of the present invention, and all modifications and equivalents of the present invention, which are made by the contents of the present specification and the accompanying drawings, or directly/indirectly applied to other related technical fields, are included in the scope of the present invention.
Claims (10)
1. The utility model provides an inboard mesa detection mechanism that sinks of part for it has the part that sinks the mesa to detect, its characterized in that includes:
the detection device comprises a base, a detection device and a detection device, wherein the base is provided with a detection table top for placing a part to be detected;
the detection support is arranged on the base and comprises an installation plate positioned above the detection table top, the installation plate is provided with an installation hole, and a first detection surface is formed on the upper surface of the installation plate; and the number of the first and second groups,
the detection pin is movably arranged in the mounting hole in the vertical direction, a second detection surface is formed on the detection pin, and the detection pin is used for moving downwards to the position where the lower end of the detection pin contacts the bottom of a sinking table surface of the part to be detected when the part to be detected is placed on the detection table surface, so that the depth deviation of the sinking table surface is measured according to the displacement change of the second detection surface relative to the first detection surface.
2. The detection mechanism for detecting the sinking platform surface at the inner side of the part as claimed in claim 1, wherein the detection pin is provided with an annular boss at the periphery, and the annular boss is positioned above the mounting plate to form a second detection surface arranged towards the mounting plate.
3. The detection mechanism for the inner side sinking platform surface of the part as claimed in claim 1, wherein the detection pin is provided in plurality, and the mounting plate is provided with a plurality of corresponding mounting holes.
4. The part inside sinker face detection mechanism of claim 1, wherein the detection bracket is rotatably mounted to the base such that the mounting plate has a detection position above the detection table and an avoidance position to avoid the detection table.
5. The part inside countertop detection mechanism of claim 1, said detection bracket further comprising:
the supporting seat is fixedly arranged on the base;
and one end of the rotating arm is rotatably arranged on the supporting seat along the vertical direction, and the mounting plate is arranged at the other end of the rotating arm.
6. The mechanism for detecting the sinking platform surface at the inner side of the part as claimed in claim 5, wherein the supporting seat is provided with a limiting part for clamping the rotating arm;
the detection support further comprises a locking piece for limiting the rotating arm to move up and down when the rotating arm rotates to be connected with the limiting portion in a clamping mode.
7. The mechanism for detecting the sinking platform surface at the inner side of the part as claimed in claim 5, wherein a position of the supporting seat connected to the rotating arm is provided with a limiting plate for limiting the rotation angle of the rotating arm in the up-down direction.
8. The mechanism for detecting the sinking platform surface at the inner side of the part as claimed in claim 1, further comprising a positioning pin for cooperating with the through hole on the part to be detected to fix the part to be detected on the detection platform surface.
9. A part inner side surface sunken table surface detection method is characterized in that the part inner side surface sunken table surface detection method is carried out by using the part inner side surface sunken table surface detection mechanism according to any one of claims 1 to 8, wherein the theoretical distance from a sunken table surface of a part to be detected to the lower surface of the mounting plate is H0The thickness of the mounting plate is H1A theoretical clearance value S is arranged between the first detection surface and the second detection surface1The second detection surface has a preset length S from the lower end of the detection pin, and S is H0+H1+S1The method for detecting the sinking platform surface on the inner side surface of the part comprises the following steps:
when the part to be detected is placed on the detection table board and the detection pin moves downwards until the lower end of the detection pin contacts the bottom of the sinking table board of the part to be detected, measuring the distance S between the first detection surface and the second detection surface2;
According to the distance S2And said theoretical clearance value S1And calculating the depth deviation of the sinking platform surface of the part to be detected.
10. The method for detecting the sinking platform surface at the inner side of the part as claimed in claim 9, wherein the distance S between the first detection surface and the second detection surface is measured when the part to be detected is placed on the detection platform surface and the detection pin moves downwards until the lower end of the detection pin contacts the bottom of the sinking platform surface of the part to be detected2The measuring tool used for measuring comprises one or more of a vernier caliper, a plug piece and a clearance gauge.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911217199.2A CN110879031A (en) | 2019-11-29 | 2019-11-29 | Detection mechanism and detection method for inner side sinking platform surface of part |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911217199.2A CN110879031A (en) | 2019-11-29 | 2019-11-29 | Detection mechanism and detection method for inner side sinking platform surface of part |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN110879031A true CN110879031A (en) | 2020-03-13 |
Family
ID=69729893
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201911217199.2A Pending CN110879031A (en) | 2019-11-29 | 2019-11-29 | Detection mechanism and detection method for inner side sinking platform surface of part |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN110879031A (en) |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3026621A (en) * | 1960-02-19 | 1962-03-27 | Joseph S Papps | Hole position gauging means |
| JP2010091302A (en) * | 2008-10-03 | 2010-04-22 | Aioi Insurance Co Ltd | Tool for measuring linear dimension |
| CN203798276U (en) * | 2014-05-08 | 2014-08-27 | 安徽江淮汽车股份有限公司 | Profile precision detection device and assembly tester |
| CN104697413A (en) * | 2015-04-02 | 2015-06-10 | 安徽江淮汽车股份有限公司 | Hole site surface difference detection device |
| CN104713446A (en) * | 2015-04-02 | 2015-06-17 | 安徽江淮汽车股份有限公司 | Plane difference detection device of concave molded surface holes |
| CN204831133U (en) * | 2015-08-07 | 2015-12-02 | 安徽江淮汽车股份有限公司 | Utensil is examined to inflation kettle installing support |
-
2019
- 2019-11-29 CN CN201911217199.2A patent/CN110879031A/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3026621A (en) * | 1960-02-19 | 1962-03-27 | Joseph S Papps | Hole position gauging means |
| JP2010091302A (en) * | 2008-10-03 | 2010-04-22 | Aioi Insurance Co Ltd | Tool for measuring linear dimension |
| CN203798276U (en) * | 2014-05-08 | 2014-08-27 | 安徽江淮汽车股份有限公司 | Profile precision detection device and assembly tester |
| CN104697413A (en) * | 2015-04-02 | 2015-06-10 | 安徽江淮汽车股份有限公司 | Hole site surface difference detection device |
| CN104713446A (en) * | 2015-04-02 | 2015-06-17 | 安徽江淮汽车股份有限公司 | Plane difference detection device of concave molded surface holes |
| CN204831133U (en) * | 2015-08-07 | 2015-12-02 | 安徽江淮汽车股份有限公司 | Utensil is examined to inflation kettle installing support |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204594373U (en) | A kind of lever measurement by magnification device | |
| CN208671901U (en) | A device for measuring two-way deviation of hole position | |
| CN205880675U (en) | Three -coordinate measuring machine part measuring uses quick aligning device | |
| CN109357582B (en) | Blade equivalent measuring tool and blade equivalent measuring method | |
| CN108253865B (en) | Rectangular groove deviation measuring instrument and measuring method | |
| CN212399000U (en) | Cradle type five-axis machine tool geometric accuracy alignment structure | |
| CN102128579B (en) | Detecting device for measuring appearance with compound angle length | |
| CN105444723B (en) | Measuring device | |
| CN218973375U (en) | Sliding door upper hinge assembly checking fixture | |
| CN207662329U (en) | The measurement cubing of the depth of parallelism between measurement rod piece difference plane | |
| CN106524881A (en) | Special calibration device for short shaft | |
| CN213842583U (en) | Multipurpose measuring tool | |
| CN210981119U (en) | Parallel roundness measuring instrument | |
| CN211601769U (en) | Measuring device | |
| CN214372123U (en) | Three-coordinate measuring support for complex parts | |
| CN222598719U (en) | Auxiliary tool for measuring inner diameter of spring washer | |
| CN219956483U (en) | Convenient height gauge | |
| CN224129479U (en) | Angle measuring device for grinding machine and grinding machine equipment | |
| CN207036070U (en) | The quick detection auxiliary smelting tool of BOSS height | |
| CN221725145U (en) | A testing fixture for mold parts | |
| CN219219132U (en) | Engineering tubular pile inclination detection device | |
| CN223339404U (en) | Concrete tile detection device | |
| CN211696209U (en) | Part perpendicularity detection gauge | |
| CN224004357U (en) | Bearing groove center diameter measuring device | |
| CN218822037U (en) | Horizontal arm small part height rapid inspection tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200313 |
|
| RJ01 | Rejection of invention patent application after publication |