CN110774057A - A special equipment for the processing of thin-walled annular cylindrical parts - Google Patents
A special equipment for the processing of thin-walled annular cylindrical parts Download PDFInfo
- Publication number
- CN110774057A CN110774057A CN201911054158.6A CN201911054158A CN110774057A CN 110774057 A CN110774057 A CN 110774057A CN 201911054158 A CN201911054158 A CN 201911054158A CN 110774057 A CN110774057 A CN 110774057A
- Authority
- CN
- China
- Prior art keywords
- processing
- thin
- special equipment
- tile
- copper
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q39/00—Metal-working machines incorporating a plurality of sub-assemblies, each capable of performing a metal-working operation
- B23Q39/02—Metal-working machines incorporating a plurality of sub-assemblies, each capable of performing a metal-working operation the sub-assemblies being capable of being brought to act at a single operating station
- B23Q39/021—Metal-working machines incorporating a plurality of sub-assemblies, each capable of performing a metal-working operation the sub-assemblies being capable of being brought to act at a single operating station with a plurality of toolheads per workholder, whereby the toolhead is a main spindle, a multispindle, a revolver or the like
- B23Q39/025—Metal-working machines incorporating a plurality of sub-assemblies, each capable of performing a metal-working operation the sub-assemblies being capable of being brought to act at a single operating station with a plurality of toolheads per workholder, whereby the toolhead is a main spindle, a multispindle, a revolver or the like with different working directions of toolheads on same workholder
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q17/00—Arrangements for observing, indicating or measuring on machine tools
- B23Q17/002—Arrangements for observing, indicating or measuring on machine tools for indicating or measuring the holding action of work or tool holders
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q3/00—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine
- B23Q3/02—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine for mounting on a work-table, tool-slide, or analogous part
- B23Q3/06—Work-clamping means
- B23Q3/062—Work-clamping means adapted for holding workpieces having a special form or being made from a special material
- B23Q3/064—Work-clamping means adapted for holding workpieces having a special form or being made from a special material for holding elongated workpieces, e.g. pipes, bars or profiles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q3/00—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine
- B23Q3/02—Devices holding, supporting, or positioning work or tools, of a kind normally removable from the machine for mounting on a work-table, tool-slide, or analogous part
- B23Q3/06—Work-clamping means
- B23Q3/08—Work-clamping means other than mechanically-actuated
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q39/00—Metal-working machines incorporating a plurality of sub-assemblies, each capable of performing a metal-working operation
- B23Q2039/002—Machines with twin spindles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q2703/00—Work clamping
- B23Q2703/02—Work clamping means
- B23Q2703/04—Work clamping means using fluid means or a vacuum
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Jigs For Machine Tools (AREA)
Abstract
本发明为一种用于薄壁环形筒件加工的专用装备,包括床身,床身上方中部固设有工作台,工作台左、右两侧各设有一套独立的且能够左右移动的加工单元;工作台上方固定安装有自动夹紧装置,自动夹紧装置包括下端固定的C型的夹具支架,压紧气缸固设于夹具支架上方,压紧气缸出轴端连接水平的连接板,连接板下方设有带有弧形面的上底座及下底座,上底座及下底座的半圆弧形面上各设有一个半圆形且配套使用的铜瓦,铜瓦凹型弧面上设有铜瓦通气槽,铜瓦上还设有用于气密检测的气密孔。该装备适用于精密薄壁筒件的两端同时加工,只要一次装夹,加工效率高,自动夹紧装置解决了加工中的装夹变形、切削变形的问题,同时减少人工因素引起的夹紧偏差,节约人力。
The invention is a special equipment for processing thin-walled annular cylindrical parts, including a bed, a worktable is fixed in the upper and middle part of the bed, and a set of independent processing machines that can move left and right are provided on the left and right sides of the worktable. Unit; an automatic clamping device is fixedly installed above the worktable, and the automatic clamping device includes a C-shaped clamp bracket fixed at the lower end. There are upper and lower bases with arc-shaped surfaces under the plate, and a semi-circular and supporting copper tile is arranged on the semi-circular arc surfaces of the upper and lower bases, and copper tiles are arranged on the concave arc surface of the copper tile. Tile ventilation groove, copper tile is also provided with airtight holes for airtight detection. The equipment is suitable for simultaneous processing of both ends of precision thin-walled cylinders. It only needs one clamping, and the processing efficiency is high. The automatic clamping device solves the problems of clamping deformation and cutting deformation during processing, and at the same time reduces the clamping caused by artificial factors. Deviation, saving manpower.
Description
(一)技术领域(1) Technical field
本发明涉及薄壁环形筒件加工设备领域,具体为一种用于薄壁环形筒件加工的专用装备。The invention relates to the field of thin-walled annular cylindrical parts processing equipment, in particular to a special equipment for thin-walled annular cylindrical parts processing.
(二)背景技术(2) Background technology
现代社会,随着科学技术的快速发展,在我国机械制造业领域内涌现出许多的精密薄壁零件,他们结构复杂,加工精度要求高,且由于精密薄壁零件刚性差,在切削力的作用下容易产生较大的让刀变形,在过大的夹紧力作用下又容易产生较大的装夹变形,用传统的装夹方法难以保证其加工精度要求。目前国内外对于精密薄壁零件的装夹和加工技术研究仍然集中在理论分析以及基础理论的研究方面,着重于在装夹技术和设备中添加新的元件以期达到较好的装夹定位和加工效果。在传统的方案分析和夹具设计中,主要依靠设计人员的经验和知识面的宽广度,分析、设计的结果可传承性比较低。In modern society, with the rapid development of science and technology, many precision thin-walled parts have emerged in the field of my country's machinery manufacturing industry. They have complex structures and high machining accuracy requirements. Due to the poor rigidity of precision thin-walled parts, they have no effect on cutting force. It is easy to produce large deformation of the knife under the action of excessive clamping force, and it is easy to produce large clamping deformation under the action of excessive clamping force. It is difficult to ensure the processing accuracy requirements with the traditional clamping method. At present, the research on the clamping and processing technology of precision thin-walled parts at home and abroad still focuses on theoretical analysis and basic theory research, focusing on adding new components to the clamping technology and equipment in order to achieve better clamping positioning and processing. Effect. In the traditional scheme analysis and fixture design, mainly relying on the designer's experience and breadth of knowledge, the results of analysis and design are less inheritable.
目前,国内外对于精密薄壁环形筒件的夹具和加工装备设计过程也类似于上述设计流程,因而也存在相同的缺陷,目前国内很少专用于加工薄壁环形筒件的自动夹具和专用设备。现有加工设备一般为普通车床,加工一端后,工件换向,再加工另一端,不能实现两端同时加工;夹具为手动锁紧夹具,重复定位精度不高;螺钉手动锁紧,夹紧力无法保证一致。At present, the design process of fixtures and processing equipment for precision thin-walled annular cylinders at home and abroad is also similar to the above design process, so there are the same defects. At present, there are few automatic fixtures and special equipment for processing thin-walled annular cylinders in China. . The existing processing equipment is generally an ordinary lathe. After processing one end, the workpiece is reversed, and then the other end is processed, and simultaneous processing of both ends cannot be achieved; the fixture is a manual locking fixture, and the repeat positioning accuracy is not high; the screw is manually locked, and the clamping force Consistency cannot be guaranteed.
(三)发明内容(3) Contents of the invention
针对以上现有技术中存在的问题,本发明提供了一种用于薄壁环形筒件加工的专用装备。In view of the above problems existing in the prior art, the present invention provides a special equipment for processing thin-walled annular cylindrical parts.
本发明是通过如下技术方案实现的:The present invention is achieved through the following technical solutions:
一种用于薄壁环形筒件加工的专用装备,包括床身,所述床身上方中部固设有工作台,所述工作台左、右两侧各设有一套独立的且能够左右移动的加工单元;所述工作台上方固定安装有自动夹紧装置,所述自动夹紧装置包括下端固定在工作台上的C型的夹具支架,所述夹具支架上端面设有通透的若干导向孔和一个气缸安装孔,压紧气缸固设于夹具支架的气缸安装孔的上方,所述压紧气缸出轴端连接有水平的连接板,导向杆一端固定在连接板上另一端穿过夹具支架上的导向孔;所述连接板下方设有能够固定环形筒件的装置。A special equipment for the processing of thin-walled annular cylindrical parts, including a bed, a worktable is fixed in the upper and middle part of the bed, and a set of independent and movable left and right sides of the worktable is provided on each of the left and right sides of the worktable. A processing unit; an automatic clamping device is fixedly installed above the worktable, and the automatic clamping device includes a C-shaped clamp bracket whose lower end is fixed on the worktable, and the upper end surface of the clamp bracket is provided with a number of transparent guide holes and a cylinder mounting hole, the pressing cylinder is fixed above the cylinder mounting hole of the fixture bracket, the outlet end of the pressing cylinder is connected with a horizontal connecting plate, one end of the guide rod is fixed on the connecting plate and the other end passes through the fixture bracket A guide hole on the upper part of the connecting plate; a device capable of fixing the annular cylinder is arranged under the connecting plate.
优选的,所述加工单元包括移动装置和加工装置,所述加工装置包括下端固定在移动装置上的电机支架、安装在电机支架上的主轴电机、通过带传动连接于所述主轴电机的主轴箱及安装在所述主轴箱出轴端的刀盘。Preferably, the processing unit includes a moving device and a processing device, the processing device includes a motor support whose lower end is fixed on the moving device, a spindle motor mounted on the motor support, and a spindle box connected to the spindle motor through a belt drive and a cutter head mounted on the shaft outlet end of the spindle box.
优选的,所述移动装置为移动滑台,包括铺设在床身上的左右方向的导轨、位于导轨上方且与导轨滑动连接的滑台、与滑台配合安装且一端转动连接于工作台一端连接有丝杠电机的丝杠。Preferably, the moving device is a mobile sliding table, which includes a guide rail laid on the bed in the left and right directions, a sliding table located above the guide rail and slidably connected to the guide rail, and a sliding table that is installed in cooperation with the sliding table and rotatably connected to the workbench at one end. The lead screw of the lead screw motor.
优选的,所述夹具支架的一侧面上安装有用于加工前确定工件轴向位置的定位气缸。Preferably, a positioning cylinder for determining the axial position of the workpiece before processing is installed on one side of the fixture bracket.
优选的,连接板下方固定环形筒件的装置包括上底座及下底座,所述上底座的上端固定连接于连接板,下底面设有半圆弧形面,所述下底座下端固定在夹具支架上,上端面设有与上底座的半圆弧形面相配合的半圆弧形面,所述上底座及下底座配套设置,在连接板下方左、右端各设有一套。Preferably, the device for fixing the annular cylinder under the connecting plate includes an upper base and a lower base, the upper end of the upper base is fixedly connected to the connecting plate, the lower bottom surface is provided with a semi-circular arc surface, and the lower end of the lower base is fixed on the clamp bracket , the upper end surface is provided with a semi-circular arc surface matching the semi-circular arc surface of the upper base.
优选的,所述上底座和下底座之间设有用于调节压紧量的调节垫板。Preferably, an adjusting pad for adjusting the pressing amount is provided between the upper base and the lower base.
优选的,上底座及下底座的半圆弧形面上各设有一个半圆形且配套使用的铜瓦,所述铜瓦上设有用于与上底座或下底座固定的筒瓦螺纹孔。Preferably, the semicircular arc surfaces of the upper base and the lower base are each provided with a semicircular copper tile which is matched with each other, and the copper tile is provided with a barrel tile threaded hole for fixing with the upper base or the lower base.
优选的,所述铜瓦的弧形凹面上设有若干个沿弧形面均布的铜瓦通气槽,铜瓦通气槽两侧形成高于铜瓦通气槽的筒瓦内接触面。Preferably, the arc-shaped concave surface of the copper tile is provided with a plurality of copper tile ventilation grooves uniformly distributed along the arc-shaped surface, and the two sides of the copper tile ventilation groove form the inner contact surface of the cylinder tile higher than the copper tile ventilation groove.
优选的,所述每片铜瓦上的铜瓦通气槽的数量为12个。Preferably, the number of copper tile ventilation grooves on each copper tile is 12.
优选的,所述铜瓦上设有开在筒瓦内接触面上的用于气密检测的气密孔。Preferably, the copper tile is provided with an airtight hole opened on the inner contact surface of the cylinder tile for airtight detection.
本发明的有益效果是:The beneficial effects of the present invention are:
本发明提供的一种用于薄壁环形筒件加工的专用装备,可满足壁厚≥0.6mm的薄壁环形筒件的一次装夹、定位,同时进行工件两端精密加工,减少了工件拆卸、装夹时间;采用自主研发的双主轴进给专用装备,带专用的加工刀盘,可同时进给,能保证工件一次装夹到位后,同时完成工件端面、内外孔倒角和切断等工序加工,大大提高了加工效率;专用夹具采用上、下压紧方式,驱动、导向部分采用气缸和直线导杆,保证上、下压紧底座精确对合,降低了操作人员手动装夹的劳动强度;上、下压紧底座分别镶有铜瓦衬套,表面设计有均匀出气槽和气密孔,保证铜瓦衬套夹持工件的均匀性和工件的安装精度,提高了加工的合格率;上底座和下底座之间设有调整垫片,调节上、下底座的压紧力;下底座设有定位气缸,对工件轴向位置精确定位;专用夹具采用气动控制、自动夹紧、气密检测,操作简单,夹紧力稳定,重复定位精度高。The special equipment for processing thin-walled annular cylindrical parts provided by the present invention can satisfy the one-time clamping and positioning of thin-walled annular cylindrical parts with a wall thickness of ≥0.6 mm, and simultaneously perform precise machining of both ends of the workpiece, thereby reducing the disassembly of the workpiece. , Clamping time; using self-developed dual-spindle feeding special equipment, with a special processing cutter head, which can be fed at the same time, which can ensure that the workpiece end face, inner and outer hole chamfering and cutting processes can be completed at the same time after the workpiece is clamped in place at one time. The processing greatly improves the processing efficiency; the special fixture adopts the upper and lower pressing methods, and the driving and guiding parts adopt the cylinder and the linear guide rod to ensure the precise alignment of the upper and lower pressing bases and reduce the labor intensity of the operator for manual clamping. ;The upper and lower pressing bases are respectively inlaid with copper tile bushings, and the surface is designed with uniform air outlet grooves and air-tight holes to ensure the uniformity of the copper tile bushings to hold the workpiece and the installation accuracy of the workpiece, and improve the qualification rate of processing; There is an adjusting gasket between the base and the lower base to adjust the pressing force of the upper and lower bases; the lower base is equipped with a positioning cylinder to precisely locate the axial position of the workpiece; the special fixture adopts pneumatic control, automatic clamping and air tightness detection , Simple operation, stable clamping force and high repeatability.
(四)附图说明(4) Description of drawings
下面结合附图对本发明作进一步的说明。The present invention will be further described below in conjunction with the accompanying drawings.
图1为现有技术加工装备结构示意图。FIG. 1 is a schematic structural diagram of a prior art processing equipment.
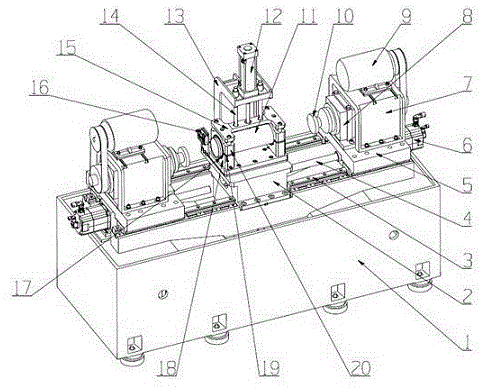
图2为本发明的整体结构示意图。FIG. 2 is a schematic diagram of the overall structure of the present invention.
图3为本发明的自动夹紧装置结构示意图。FIG. 3 is a schematic structural diagram of the automatic clamping device of the present invention.
图4为本发明的铜瓦结构示意图。FIG. 4 is a schematic diagram of the structure of the copper tile of the present invention.
图中,1-床身、2-工作台、3-导轨、4-丝杠、5-滑台、6-丝杠电机、7-电机支架、8-主轴箱、9-主轴电机、10-刀盘、11-工件、12-压紧气缸、13-夹具支架、14-导向杆、15-连接板、16-定位气缸、17-铜瓦、18-下底座、19-调节垫片、20-上底座、A-气密孔、B-铜瓦螺纹孔、C-铜瓦通气槽、D-铜瓦内接触面。In the figure, 1-bed, 2-table, 3-guide, 4-screw, 5-slide, 6-screw motor, 7-motor bracket, 8-spindle box, 9-spindle motor, 10- Cutter head, 11-workpiece, 12-pressing cylinder, 13-fixture bracket, 14-guide rod, 15-connecting plate, 16-positioning cylinder, 17-copper tile, 18-lower base, 19-adjusting gasket, 20 - Upper base, A-airtight hole, B-copper tile threaded hole, C-copper tile ventilation groove, D-copper tile inner contact surface.
(五)具体实施方式(5) Specific implementation methods
为使本领域技术人员能够更好的理解本发明,下面将结合附图1-4对本发明技术方案做进一步的说明。In order to enable those skilled in the art to better understand the present invention, the technical solutions of the present invention will be further described below with reference to the accompanying drawings 1-4.
参照图1至图4所示,本发明为一种用于薄壁环形筒件加工的专用装备,包括床身1,床身1上方中部固设有工作台2,工作台2左、右两侧各设有一套独立的且能够左右移动的加工单元,加工单元包括移动装置和加工装置,加工装置包括下端固定在移动装置上的电机支架7、安装在电机支架7上的主轴电机9、通过带传动连接于所述主轴电机9的主轴箱8及安装在所述主轴箱8出轴端的刀盘10,主轴电机9通过带传动带动主轴箱8转动,进而带动刀盘10的转动,转动的同时通过移动装置左右移动进给,完成工件端面、内外孔倒角和切断等工序加工。1 to 4, the present invention is a special equipment for processing thin-walled annular cylindrical parts, including a bed 1, a workbench 2 is fixed in the upper middle of the bed 1, and the left and right sides of the workbench 2 are Each side is provided with a set of independent processing units that can move left and right. The processing unit includes a mobile device and a processing device. The processing device includes a motor bracket 7 whose lower end is fixed on the mobile device, and a spindle motor 9 installed on the motor bracket 7. The belt drive is connected to the spindle box 8 of the spindle motor 9 and the cutter head 10 installed at the outlet end of the spindle box 8. The spindle motor 9 drives the spindle box 8 to rotate through the belt drive, thereby driving the rotation of the cutter head 10. At the same time, the moving device moves left and right to feed, and completes the process of workpiece end face, inner and outer hole chamfering and cutting.
移动装置为移动滑台,包括铺设在床身1上的左右方向的导轨3、位于导轨3上方且与导轨3滑动连接的滑台5、与滑台5配合安装且一端转动连接于工作台2一端连接有丝杠电机6的丝杠4,移动滑台和加工装置配套,在工作台2左、右两侧各一套,左、右的加工装置在下方的移动滑台的带动下,能够同时对工件左右两端进行工件端面、内外孔倒角和切断工序,不需要换头重新装夹。移动滑台在控制系统控制下通过丝杠电机6带动能够精确的定位移动位置,保证加工进给量。The moving device is a moving slide table, including a guide rail 3 laid on the bed 1 in the left and right directions, a slide table 5 located above the guide rail 3 and slidably connected to the guide rail 3, and installed in cooperation with the slide table 5 and one end of which is rotatably connected to the workbench 2. One end is connected with the lead screw 4 of the lead screw motor 6. The mobile sliding table is matched with the processing device. One set is on the left and right sides of the workbench 2. The left and right processing devices are driven by the mobile sliding table below. At the same time, the workpiece end face, inner and outer hole chamfering and cutting processes are performed on the left and right ends of the workpiece, and there is no need to change the head and re-clamping. The moving slide is driven by the screw motor 6 under the control of the control system to accurately locate the moving position and ensure the processing feed.
工作台2上方固定安装有自动夹紧装置(如图3所述),自动夹紧装置包括下端固定在工作台2上的C型的夹具支架13,夹具支架13上端面设有通透的若干导向孔和一个气缸安装孔,在本实施例中导向孔数量为两个,关于气缸安装孔左右对称,压紧气缸12固设于夹具支架13的气缸安装孔的上方,与气缸安装孔同轴设置,压紧气缸12伸出轴通过气缸安装孔,且出轴端固定连接有水平的连接板15,导向杆14下端固定在连接板15上,另一端穿过夹具支架13上的导向孔,导向杆14与压紧气缸12伸出轴空间平行,起到上下导向作用,保证压紧用于夹紧工件的上、下压紧底座精确对合。An automatic clamping device (as shown in Figure 3) is fixedly installed above the workbench 2. The automatic clamping device includes a C-
连接板15下方设有能够固定环形筒件的装置,包括上底座20及下底座18,上底座20的上端固定连接于连接板15,下底面设有半圆弧形面,所述下底座18下端固定在夹具支架13上,上端面设有与上底座20的半圆弧形面相配合的半圆弧形面,上底座20及下底座18配套设置,用来夹持环形筒件,在连接板15下方左、右端各设有一套,保证夹紧的稳定性。Below the connecting
上底座20和下底座18之间设有用于调节压紧量的调节垫板19。Between the
上底座20及下底座18的半圆弧形面上各设有一个半圆形且配套使用的铜瓦17,所述铜瓦17上设有用于与上底座20或下底座18固定的筒瓦螺纹孔B,每个筒瓦17上设有共6个螺钉,左、右、中各两个,保证筒瓦17固定的精确位置。筒瓦17易于更换,上底座20及下底座18可以适应±5mm内不同内径的筒瓦17的安装,以适应更多型号的环形筒件的夹持固定及加工,有更高的实用性。The semicircular arc surfaces of the
铜瓦17的弧形凹面上设有12个沿弧形面均布的铜瓦通气C,铜瓦通气槽C两侧形成高于铜瓦通气槽C的筒瓦内接触面D,铜瓦通气槽C中允许空气进入,能够平衡薄壁筒件内、外压力;筒瓦内接触面D与工件实际接触,能够保证加持力的平衡和稳定。The curved concave surface of the
铜瓦17上设有开在筒瓦内接触面D上的用于气密检测的气密孔A,气密孔A设有对称的两个,通过检测气密性来判断筒瓦内接触面D是否完全贴紧工件,保证夹紧时的同轴度。The
夹具支架13的一侧面上安装有用于加工前确定工件轴向位置的定位气缸16,在加工前伸出,工件的一端贴紧,然后再固定工件,收回气缸,保证气缸的轴向位置,进而保障加工的位置精度。A
图1为现有技术的加工设备的参考图。FIG. 1 is a reference diagram of a prior art processing equipment.
工作工程如下:初始状态为压紧气缸12升起、定位气缸16退回的状态;开始工作时,定位气缸16伸出,操作人员将工件11放在下底座17上,保证左侧与伸出的定位气缸16接触;压紧气缸下落压紧固定工件,检测气密性;气密性正常,定位气缸16退回,开始左、右加工;加工完成后,压紧气缸12升起,取出工件,进行下一个工件的加工。The working process is as follows: the initial state is that the pressing cylinder 12 is raised and the
本发明的描述中,术语“上”、“下”、“前”、“后”、“左”、“右”、“顶”、“底”、“竖直”、“水平”等指示的方位或位置关系为基于附图所示的方位或位置关系(如在本发明中,以图2的方位或位置关系进行描述),仅是为了描述本发明而不是要求本发明必须以特定的方位构造或操作,因此不能理解为对本发明的限制。本发明中的“相连”“连接”应作广义理解,例如,可以是连接,也可以是可拆卸连接;可以是直接连接,也可以是通过中间部件间接连接,对于本领域的普通技术人员而言,可以具体情况理解上述术语的具体含义。In the description of the present invention, the terms "upper", "lower", "front", "rear", "left", "right", "top", "bottom", "vertical", "horizontal", etc. The orientation or positional relationship is based on the orientation or positional relationship shown in the accompanying drawings (for example, in the present invention, the orientation or positional relationship in FIG. 2 is described), which is only for describing the present invention and does not require the present invention to be in a specific orientation. construction or operation, and therefore should not be construed as limiting the invention. In the present invention, "connected" and "connected" should be understood in a broad sense, for example, it may be a connection or a detachable connection; it may be a direct connection or an indirect connection through an intermediate component. In other words, the specific meanings of the above terms can be understood in specific situations.
以上所述为本发明的优选实施方式,具体实施例的说明仅用于更好的理解本发明的思想。对于本技术领域的普通技术人员来说,依照本发明原理还可以做出若干改进或者同等替换,这些改进或同等替换也视为落在本发明的保护范围。The above descriptions are the preferred embodiments of the present invention, and the description of the specific embodiments is only used to better understand the idea of the present invention. For those skilled in the art, several improvements or equivalent replacements can also be made according to the principles of the present invention, and these improvements or equivalent replacements are also considered to fall within the protection scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911054158.6A CN110774057A (en) | 2019-10-31 | 2019-10-31 | A special equipment for the processing of thin-walled annular cylindrical parts |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201911054158.6A CN110774057A (en) | 2019-10-31 | 2019-10-31 | A special equipment for the processing of thin-walled annular cylindrical parts |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN110774057A true CN110774057A (en) | 2020-02-11 |
Family
ID=69388207
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201911054158.6A Pending CN110774057A (en) | 2019-10-31 | 2019-10-31 | A special equipment for the processing of thin-walled annular cylindrical parts |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN110774057A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119973621A (en) * | 2025-02-13 | 2025-05-13 | 中核(天津)科技发展有限公司 | Thin-walled parts assembly device and method |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20040194967A1 (en) * | 2003-02-27 | 2004-10-07 | Manfred Jaensch | Insert for gripping apparatus |
| CN202571944U (en) * | 2012-03-15 | 2012-12-05 | 天长市曙光电子有限公司 | Clamp used for hydraulic horizontal type broaching machine |
| CN203209977U (en) * | 2012-12-28 | 2013-09-25 | 云南丽江机床有限公司 | Machine tool for machining barrel body |
| CN103541669A (en) * | 2013-10-25 | 2014-01-29 | 镇江安达煤矿专用设备有限公司 | Split type slip |
| CN104259900A (en) * | 2014-09-26 | 2015-01-07 | 中核(天津)机械有限公司 | Thin-walled cylindrical part end face machining fixture |
| CN104712284A (en) * | 2013-12-14 | 2015-06-17 | 江苏贵鑫石油装备有限公司 | Liquid-operated reducing oil tube clamping blowout preventer |
| CN208358346U (en) * | 2018-07-02 | 2019-01-11 | 苏州优达科精密机械有限公司 | A kind of gas picks up formula stationary fixture |
| CN208961841U (en) * | 2018-09-21 | 2019-06-11 | 上海径驰模具制造有限公司 | A kind of drying fixture |
| CN211136238U (en) * | 2019-10-31 | 2020-07-31 | 滨州渤海活塞有限公司 | Special boring machine for thin-wall annular cylinder part |
-
2019
- 2019-10-31 CN CN201911054158.6A patent/CN110774057A/en active Pending
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20040194967A1 (en) * | 2003-02-27 | 2004-10-07 | Manfred Jaensch | Insert for gripping apparatus |
| CN202571944U (en) * | 2012-03-15 | 2012-12-05 | 天长市曙光电子有限公司 | Clamp used for hydraulic horizontal type broaching machine |
| CN203209977U (en) * | 2012-12-28 | 2013-09-25 | 云南丽江机床有限公司 | Machine tool for machining barrel body |
| CN103541669A (en) * | 2013-10-25 | 2014-01-29 | 镇江安达煤矿专用设备有限公司 | Split type slip |
| CN104712284A (en) * | 2013-12-14 | 2015-06-17 | 江苏贵鑫石油装备有限公司 | Liquid-operated reducing oil tube clamping blowout preventer |
| CN104259900A (en) * | 2014-09-26 | 2015-01-07 | 中核(天津)机械有限公司 | Thin-walled cylindrical part end face machining fixture |
| CN208358346U (en) * | 2018-07-02 | 2019-01-11 | 苏州优达科精密机械有限公司 | A kind of gas picks up formula stationary fixture |
| CN208961841U (en) * | 2018-09-21 | 2019-06-11 | 上海径驰模具制造有限公司 | A kind of drying fixture |
| CN211136238U (en) * | 2019-10-31 | 2020-07-31 | 滨州渤海活塞有限公司 | Special boring machine for thin-wall annular cylinder part |
Non-Patent Citations (1)
| Title |
|---|
| 陆祥生等编: "机械手理论及应用", 31 March 1985, 中国铁道出版社, pages: 203 * |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN119973621A (en) * | 2025-02-13 | 2025-05-13 | 中核(天津)科技发展有限公司 | Thin-walled parts assembly device and method |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN210080831U (en) | A positioning and cutting device for steel pipe processing | |
| CN109732272B (en) | Full ceramic bearing electricity main shaft bearing and pivot dismounting device | |
| CN111823036B (en) | Rapid positioning device and method for thin-walled cone | |
| CN106238769A (en) | The drilling equipment of a kind of plate and method | |
| CN213858193U (en) | Turning and milling positioning device of numerical control milling machine | |
| CN211728447U (en) | A horizontal machining center fixture mechanism | |
| CN219211825U (en) | A step-by-step pipe automatic cutting device | |
| CN203831132U (en) | Locating seat | |
| CN202123582U (en) | Self-centring synchronous clamping device of silicon rod | |
| CN211136238U (en) | Special boring machine for thin-wall annular cylinder part | |
| CN116423412B (en) | A thin-walled cylindrical workpiece processing and positioning device | |
| CN219233998U (en) | A Quick Positioning Boring Machine | |
| CN217019513U (en) | Auxiliary clamping component of numerical control machine tool | |
| CN205309934U (en) | A multi-axis linkage numerical control equipment with adjustable feeding angle | |
| CN211639174U (en) | An automatic clamping device specially used for processing dragon tendon ingot holes and planes | |
| CN204603886U (en) | A kind of quick change clamping device | |
| CN207900268U (en) | A kind of small drilling machine | |
| CN223186086U (en) | A fixture device for a vertical five-axis machine | |
| CN218983205U (en) | Positioning fixture for numerical control lathe machining | |
| CN219189412U (en) | Automatic positioning fixture of numerical control machine tool | |
| CN219404627U (en) | A Quick Centering Auxiliary Fixture for Milling Machine | |
| CN219484330U (en) | Automatic centering, positioning and clamping device for milling machine machining | |
| CN223889793U (en) | Workpiece clamping tool | |
| CN209919376U (en) | A kind of butterfly valve butterfly plate processing tool | |
| CN221290290U (en) | Boring and milling clamp device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20200211 |
|
| RJ01 | Rejection of invention patent application after publication |