CN110640632B - Polishing method - Google Patents

Polishing method Download PDF

Info

Publication number
CN110640632B
CN110640632B CN201910938403.3A CN201910938403A CN110640632B CN 110640632 B CN110640632 B CN 110640632B CN 201910938403 A CN201910938403 A CN 201910938403A CN 110640632 B CN110640632 B CN 110640632B
Authority
CN
China
Prior art keywords
disc
fan
bodies
disc body
abrasive
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Active
Application number
CN201910938403.3A
Other languages
Chinese (zh)
Other versions
CN110640632A (en
Inventor
赵薇
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
Zhejiang Luoke Photoelectric Technology Co ltd
Original Assignee
Jinghailianke Ningbo Intelligent Equipment Co ltd
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by Jinghailianke Ningbo Intelligent Equipment Co ltd filed Critical Jinghailianke Ningbo Intelligent Equipment Co ltd
Priority to CN201910938403.3A priority Critical patent/CN110640632B/en
Publication of CN110640632A publication Critical patent/CN110640632A/en
Application granted granted Critical
Publication of CN110640632B publication Critical patent/CN110640632B/en
Active legal-status Critical Current
Anticipated expiration legal-status Critical

Links

Images

Classifications

    • BPERFORMING OPERATIONS; TRANSPORTING
    • B24GRINDING; POLISHING
    • B24BMACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
    • B24B55/00Safety devices for grinding or polishing machines; Accessories fitted to grinding or polishing machines for keeping tools or parts of the machine in good working condition
    • B24B55/06Dust extraction equipment on grinding or polishing machines
    • BPERFORMING OPERATIONS; TRANSPORTING
    • B24GRINDING; POLISHING
    • B24BMACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
    • B24B41/00Component parts such as frames, beds, carriages, headstocks
    • B24B41/007Weight compensation; Temperature compensation; Vibration damping
    • BPERFORMING OPERATIONS; TRANSPORTING
    • B24GRINDING; POLISHING
    • B24BMACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
    • B24B41/00Component parts such as frames, beds, carriages, headstocks
    • B24B41/04Headstocks; Working-spindles; Features relating thereto
    • BPERFORMING OPERATIONS; TRANSPORTING
    • B24GRINDING; POLISHING
    • B24BMACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
    • B24B45/00Means for securing grinding wheels on rotary arbors
    • B24B45/003Accessories therefor

Landscapes

  • Engineering & Computer Science (AREA)
  • Mechanical Engineering (AREA)
  • Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)

Abstract

本发明公开了一种抛光方法,在第一盘体(53)和第三盘体(63)上分别安装不同型号的磨料盘(50),如可在第一盘体(53)上安装型号一的磨料盘(50),在第三盘体(63)上安装型号二的磨料盘(50),组装时,滑动连接头(61)滑动卡入在槽盘连接管(51)内,使第一盘体(53)位于第二扇形孔(64),且第一盘体(53)的底面与第三盘体(63)的底面处于不同的水平面上,每个第二盘体(54)分别对应贴靠在第三盘体(63)上,第一盘体和第三盘体的底面分别固定有磨料盘;本发明能够实现自动更换磨料盘,无需人工拆卸更换,大大提高打磨抛光的效率,适用于大规模打磨抛光工作。
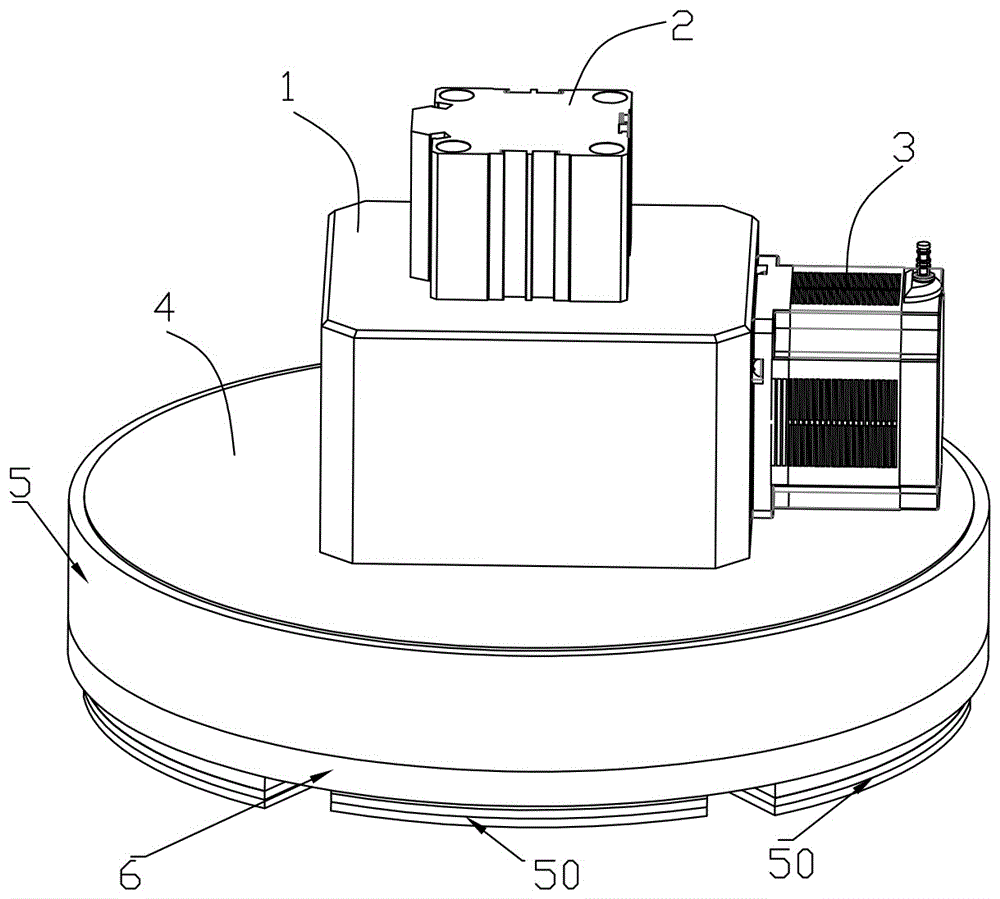
Figure 201910938403

The invention discloses a polishing method. Abrasive discs (50) of different types are respectively installed on a first disc body (53) and a third disc body (63). The abrasive disc (50) of the first type is installed on the third disc body (63), and the abrasive disc (50) of type 2 is installed on the third disc body (63). The first disc body (53) is located in the second fan-shaped hole (64), and the bottom surface of the first disc body (53) and the bottom surface of the third disc body (63) are on different horizontal planes, and each second disc body (54) ) are respectively attached to the third disc body (63), and the bottom surfaces of the first disc body and the third disc body are respectively fixed with abrasive discs; the present invention can realize automatic replacement of abrasive discs without manual disassembly and replacement, and greatly improves grinding and polishing. The efficiency is suitable for large-scale grinding and polishing work.

Figure 201910938403

Description

Polishing method
Technical Field
The invention relates to the technical field of grinding and polishing equipment, in particular to a polishing method.
Background
When the surface of a workpiece is polished, abrasive discs of different models are required to be replaced to finish polishing, and the polishing is finished by manually disassembling the abrasive discs at present, so that the polishing efficiency is low, time and labor are wasted, and the polishing tool is not suitable for large-scale polishing.
Disclosure of Invention
The object of the present invention is to overcome the above-mentioned disadvantages and to provide a polishing method.
In order to achieve the purpose, the invention adopts the following specific scheme:
a polishing method comprises a driving support frame, a lifting cylinder, a rotary driving motor, a sealing cover disc, a rotary groove disc and a sliding disc, wherein the driving support frame is fixed on the sealing cover disc, the lifting cylinder is fixed on the top surface of the driving support frame, the rotary driving motor is fixed on the side surface of the driving support frame, the output end of the lifting cylinder extends into the driving support frame and is connected with a first connecting shaft, the other end of the first connecting shaft is connected with one end of a second connecting shaft through a first bearing, the output end of the rotary driving motor extends into the driving support frame and is connected with a driving bevel gear, the rotary groove disc comprises a groove disc connecting pipe, an annular enclosure, three fan-shaped first disc bodies and three fan-shaped second disc bodies, and the two ends of the three first disc bodies are respectively connected to the inner wall of the annular enclosure and the outer wall of the lower end of the groove disc connecting pipe, the two ends of the three second disc bodies are respectively connected to the inner wall of the annular enclosure and the outer wall of the lower end of the groove disc connecting pipe, the three first disc bodies and the three second disc bodies are arranged at intervals, the thickness of the first disc body is larger than that of the second disc body, a first fan-shaped hole is formed between the first disc body and the second disc body, the upper end of the groove disc connecting pipe penetrates through the sealing cover disc and then is fixedly sleeved with a driven conical gear, the driven conical gear is meshed with the driving conical gear, the groove disc connecting pipe is further connected with the sealing cover disc through a second bearing, a dust storage cavity is formed between the rotary groove disc and the sealing cover disc, a vacuum suction nozzle communicated with the dust storage cavity is arranged on the sealing cover disc, the sliding disc comprises a sliding connector, an enclosure ring and three third disc bodies, the sliding connector extends into the groove disc connecting pipe and is connected with the groove disc connecting pipe in a sliding mode in the rotating direction, the other end of second connecting axle stretches into in the groove dish connecting tube to with sliding connection head fixed connection, three the both ends of third disk body are connected respectively on inner wall and the sliding connection head of enclosing the retaining ring, three the third disk body partition encloses the retaining ring, adjacent two be formed with between the third disk body with first disk body complex second fan-shaped hole, every it is equipped with two fan-shaped lugs to correspond first fan-shaped hole on the third disk body, fan-shaped lug is equipped with the absorption hole along radial interval, absorption hole and dust storage cavity intercommunication, the bottom surface of first disk body and third disk body is fixed with sectorial abrasive material dish respectively, the abrasive material dish is used for polishing workpiece surface.
Wherein the abrasive disc comprises a shock absorbing foam pad and an abrasive block.
The inner wall of the groove plate connecting pipe is provided with a key groove, and the outer wall of the sliding connector is provided with a sliding key corresponding to the key groove.
The invention has the beneficial effects that: compared with the prior art, the grinding material discs of different models are respectively arranged on the rotary groove disc and the sliding disc, the sliding disc is driven to ascend and descend by the pulling cylinder, the automatic grinding material disc replacement is realized, manual disassembly and replacement are not needed, the grinding and polishing efficiency is greatly improved, the production efficiency is improved, the time is saved, the structure is more automatic, and the grinding and polishing device is suitable for large-scale grinding and polishing work;
in addition, in the grinding and polishing process, the chips and powder generated by grinding can be automatically cleaned, the polishing effect of the surface of the workpiece is guaranteed, the polishing effect is better, extra cleaning equipment is not needed, and the grinding and polishing cost is reduced.
Drawings
Fig. 1 is a schematic structural diagram of a polishing mechanism provided in an embodiment of the present invention;
FIG. 2 is a cross-sectional view of a polishing mechanism provided in an embodiment of the present invention;
FIG. 3 is an exploded view of a polishing mechanism provided in accordance with an embodiment of the present invention;
FIG. 4 is a schematic diagram of a polishing mechanism according to an embodiment of the present invention from another perspective;
FIG. 5 is a diagram of a polishing mechanism according to an embodiment of the present invention after replacing an abrasive disc;
FIG. 6 is a schematic structural diagram of a rotary fluted disc provided by an embodiment of the invention;
FIG. 7 is a structural diagram of another view of a rotating grooved disk according to an embodiment of the present invention;
FIG. 8 is a schematic structural diagram of a slider tray provided in an embodiment of the present invention;
FIG. 9 is a schematic structural diagram of another perspective of a slider tray according to an embodiment of the present invention;
FIG. 10 is a schematic view of a configuration of a rotating grooved disk and a sliding disk according to an embodiment of the present invention;
FIG. 11 is a schematic structural view of another perspective of the engagement of a rotating slotted disk with a sliding disk according to an embodiment of the present invention;
description of reference numerals: 1-driving a support frame; 2-pulling up the cylinder; 3-rotating the drive motor; 4-closing the cover disc; 5-rotating the grooved disc; 51-groove disk connecting pipe; 52-annular enclosure; 53-first tray; 54-a second tray; 55-a first sector aperture; 6-sliding disc; 61-sliding connection head; 62-a surrounding check ring; 63-a third tray; 64-a second sector aperture; 65-sector bumps; 66-adsorption pores; 7-a first connecting shaft; 8-a first bearing; 9-a second connecting shaft; 10-driving bevel gear; 20-driven bevel gear; 30-a second bearing; 40-a dust storage chamber; 50-abrasive discs; 501-a shock-absorbing sponge cushion; 502-abrasive block.
Detailed Description
The invention will be described in further detail with reference to the following figures and specific examples, without limiting the scope of the invention.
As shown in fig. 1 to 11, a polishing method according to this embodiment includes a driving support frame 1, a pulling cylinder 2, a rotary driving motor 3, a capping disc 4, a rotary trough disc 5 and a sliding disc 6, where the driving support frame 1 is fixed on the capping disc 4, the pulling cylinder 2 is fixed on the top surface of the driving support frame 1, the rotary driving motor 3 is fixed on the side surface of the driving support frame 1, an output end of the pulling cylinder 2 extends into the driving support frame 1 and is connected to a first connecting shaft 7, another end of the first connecting shaft 7 is connected to one end of a second connecting shaft 9 through a first bearing 8, an output end of the rotary driving motor 3 extends into the driving support frame 1 and is connected to a driving bevel gear 10, the rotary trough disc 5 includes a trough disc connecting pipe 51, an annular enclosure 52, three fan-shaped first disc bodies 53 and three fan-shaped second disc bodies 54, the two ends of the three first disc bodies 53 are respectively connected to the inner wall of the annular enclosure 52 and the outer wall of the lower end of the groove disc connecting pipe 51, the two ends of the three second disc bodies 54 are respectively connected to the inner wall of the annular enclosure 52 and the outer wall of the lower end of the groove disc connecting pipe 51, the three first disc bodies 53 and the three second disc bodies 54 are arranged at intervals, namely the first disc bodies 53 and the second disc bodies 54 are arranged in a staggered manner, the thickness of the first disc bodies 53 is larger than that of the second disc bodies 54, first fan-shaped holes 55 are formed between the first disc bodies 53 and the second disc bodies 54, namely six first fan-shaped holes 55 are formed, the driven conical gear 20 is fixedly sleeved at the upper end of the groove disc connecting pipe 51 after penetrating through the cover disc 4, the driven conical gear 20 is meshed with the driving conical gear 10, the groove disc connecting pipe 51 is further connected with the cover disc 4 through the second bearing 30, and a dust storage chamber 40 is formed between the rotating groove disc 5 and the cover disc 4, be equipped with the vacuum nozzle (not shown in the figure) that communicates with dust storage cavity 40 on the closing cap disc 4, sliding disk 6 includes sliding connection head 61, encloses retaining ring 62 and three third disk 63, sliding connection head 61 stretches into in groove dish connecting pipe 51 to with groove dish connecting pipe 51 slip joint in the direction of rotation, the other end of second connecting axle 9 stretches into in groove dish connecting pipe 51, and with sliding connection head 61 fixed connection, three the both ends of third disk 63 are connected respectively on the inner wall and the sliding connection head 61 that enclose retaining ring 62, three retaining ring 62 is enclosed to the third disk 63 partition, be formed with between two adjacent third disk 63 with first disk 53 complex second fan-shaped hole 64, every be equipped with two fan-shaped lugs 65 corresponding first fan-shaped hole 55 on the third disk 63, fan-shaped lug 65 is equipped with adsorption hole 66 along radial interval, the absorption hole 66 communicates with the dust storage chamber 40, the bottom surfaces of the first tray body 53 and the third tray body 63 are respectively fixed with the fan-shaped abrasive disc 50, optionally, a model bump matched with the size and the shape of the abrasive disc 50 is arranged on the bottom surface of the third tray body 63, the abrasive disc 50 is fixed on the model bump, so that the abrasive disc 50 and the absorption hole 66 have a height difference, the absorption hole 66 is favorable for absorbing chips and powder, and the abrasive disc 50 is used for polishing the surface of a workpiece.
Specifically, according to the actual polishing requirement, abrasive discs 50 of different types are respectively mounted on the first disc 53 and the third disc 63, for example, abrasive discs 50 of a first type can be mounted on the first disc 53, abrasive discs 50 of a second type are mounted on the third disc 63, during assembly, the sliding connector 61 is slidably clamped in the slot disc connecting pipe 51, so that the first disc 53 is located in the second fan-shaped hole 64, the bottom surface of the first disc 53 and the bottom surface of the third disc 63 are located on different horizontal planes, each second disc 54 is correspondingly attached to the third disc 63 and located between two fan-shaped protrusions 65, each fan-shaped protrusion 65 is correspondingly and movably inserted into each first fan-shaped hole 55, and the top surface of each fan-shaped protrusion 65 is higher than the top surface of the second disc 54, during operation, the rotary driving motor 3 drives the driving bevel gear 10 to rotate, the driving bevel gear 10 drives the driven bevel gear 20 to rotate, the driven bevel gear 20 drives the rotary groove disc 5 to rotate, the rotary groove disc 5 drives the sliding disc 6 to rotate, the bottom surface of the first disc body 53 and the bottom surface of the third disc body 63 are positioned on different horizontal planes, therefore, when the rotary groove disc 5 rotates, the abrasive disc 50 on the first disc body 53 or the abrasive disc 50 on the third disc body 63 can be in contact with the surface of a workpiece to polish the surface of the workpiece, according to the polishing processing sequence, the abrasive disc 50 of the first type on the first disc body 53 polishes the surface of the workpiece, namely the bottom surface of the first disc body 53 is lower than the bottom surface of the third disc body 63, then the abrasive disc 50 of the second type on the third disc body 63 is used to polish the surface of the workpiece, at the moment, the lifting cylinder 2 works to drive the first connecting shaft 7 to extend downwards, the first connecting shaft 7 pushes the second connecting shaft 9 to move downwards, the second connecting shaft 9 pushes the sliding disc 6 to move downwards, the height of the bottom surface of the third disc body 63 is lower than that of the bottom surface of the first disc body 53, and the height of the top surface of the fan-shaped bump 65 is not lower than that of the top surface of the second disc body 54, so that the work of switching the abrasive disc 50 of the first type to the abrasive disc 50 of the second type is automatically completed, the abrasive disc is convenient and quick, and after the abrasive disc 50 of the second type is polished, the sliding disc 6 is driven to return by pulling the first connecting shaft 7 and the second connecting shaft 9 through the pulling cylinder 2, so that the abrasive disc 50 of the first type is located at the working position, the first connecting shaft 7 is connected with the second connecting shaft 9 through the first bearing 8, and the sliding disc 6 cannot drive the first connecting shaft 7 to rotate in the rotating process; simultaneously at the burnishing and polishing in-process, through vacuum nozzle to storing up dirt cavity 40 evacuation processing, under negative pressure state, the piece and the powder of the production of polishing are inhaled in storing up dirt cavity 40 through absorption hole 66, so realize the clearance to the workpiece surface, avoid piece and powder to influence polishing effect.
And to the work piece that needs the abrasive disc 50 of a model can accomplish polishing, the accessible draws the bottom surface height that rises cylinder 2 adjustment third dish 63 and the bottom surface height of first dish 53 to the abrasive disc 50 of the same model of installation is polished workpiece surface, thereby can improve polishing's efficiency, and the structure is nimble.
In the embodiment, abrasive discs 50 of different types can be respectively arranged on the rotary groove disc 5 and the sliding disc 6, the sliding disc 6 is driven to ascend and descend by the pulling cylinder 2, the automatic replacement of the abrasive discs 50 is realized, manual disassembly and replacement are not needed, the grinding and polishing efficiency is greatly improved, the production efficiency is improved, the time is saved, the structure is more automatic, and the grinding and polishing device is suitable for large-scale grinding and polishing work;
in addition, in the grinding and polishing process, the chips and powder generated by grinding can be automatically cleaned, the polishing effect of the surface of the workpiece is guaranteed, the polishing effect is better, extra cleaning equipment is not needed, and the grinding and polishing cost is reduced.
Based on the above embodiments, further, as shown in fig. 3, the abrasive disc 50 includes a shock-absorbing sponge 501 and an abrasive block 502; specifically, the damping foam-rubber cushion 501 is fixed on the bottom surfaces of the first disc body 53 and the third disc body 63 correspondingly, the abrasive block 502 is fixed on the damping foam-rubber cushion 501 correspondingly, in the working process, the abrasive block 502 polishes and polishes the surface of a workpiece, and the damping foam-rubber cushion 501 provides a buffering effect for the abrasive block 502, so that the abrasive block 502 can be better protected, and the service life of the abrasive block 502 is prolonged.
Based on the above embodiment, further, a key slot is arranged on the inner wall of the slot disc connecting pipe 51, and a sliding key is arranged on the outer wall of the sliding connector 61 corresponding to the key slot; specifically, key grooves are arranged on the inner circumferential wall of the tray connecting pipe 51 at equal intervals, correspondingly, sliding keys are arranged on the outer circumferential wall of the sliding connecting head 61 at equal intervals, during installation, the sliding keys on the sliding connecting head 61 correspond to the key grooves of the tray connecting pipe 51 and then slide into the tray connecting pipe 51, so that the sliding connecting head 61 and the tray connecting pipe 51 are clamped in the rotating direction, and the sliding disc 6 rotates along with the rotating tray 5 under the driving of the rotating tray 5, so that the grinding disc 50 on the sliding disc 6 polishes the surface of a workpiece.
The above description is only a preferred embodiment of the present invention, and all equivalent changes or modifications of the structure, characteristics and principles described in the present patent application are included in the protection scope of the present patent application.

Claims (1)

1. A polishing method is characterized by comprising a driving support frame, a lifting cylinder, a rotary driving motor, a sealing disc, a rotary groove disc and a sliding disc, wherein the driving support frame is fixed on the sealing disc, the lifting cylinder is fixed on the top surface of the driving support frame, the rotary driving motor is fixed on the side surface of the driving support frame, the output end of the lifting cylinder extends into the driving support frame and is connected with a first connecting shaft, the other end of the first connecting shaft is connected with one end of a second connecting shaft through a first bearing, the output end of the rotary driving motor extends into the driving support frame and is connected with a driving bevel gear, the rotary groove disc comprises a groove disc connecting pipe, an annular enclosure, three fan-shaped first disc bodies and three fan-shaped second disc bodies, the two ends of the three first disc bodies are respectively connected to the inner wall of the annular enclosure and the outer wall of the lower end of the groove disc connecting pipe, the two ends of the three second disc bodies are respectively connected to the inner wall of the annular enclosure and the outer wall of the lower end of the groove disc connecting pipe, the three first disc bodies and the three second disc bodies are arranged at intervals, namely the first disc bodies and the second disc bodies are arranged in a staggered manner, the thickness of the first disc bodies is larger than that of the second disc bodies, a first fan-shaped hole is formed between the first disc bodies and the second disc bodies, namely six first fan-shaped holes, the upper end of the groove disc connecting pipe penetrates through the sealing disc and then is fixedly sleeved with a driven conical gear, the driven conical gear is meshed with the driving conical gear, the groove disc connecting pipe is further connected with the sealing disc through a second bearing, a dust storage cavity is formed between the rotating groove disc and the sealing disc, the sealing disc is provided with a vacuum suction nozzle communicated with the dust storage cavity, and the sliding disc comprises a sliding connector, an enclosure ring and three third disc bodies, the sliding connector stretches into the groove disc connecting pipe and is connected with the groove disc connecting pipe in a sliding and clamping mode in the rotating direction, the other end of the second connecting shaft stretches into the groove disc connecting pipe and is fixedly connected with the sliding connector, the two ends of the three third disc bodies are respectively connected to the inner wall of the enclosing check ring and the sliding connector, the three third disc bodies are equally divided into the enclosing check ring, a second fan-shaped hole matched with the first disc body is formed between every two adjacent third disc bodies, two fan-shaped convex blocks are arranged on each third disc body corresponding to the first fan-shaped hole, the fan-shaped convex blocks are provided with adsorption holes along the radial direction at intervals, the adsorption holes are communicated with a dust storage cavity, the bottom surfaces of the first disc body and the third disc bodies are respectively fixed with fan-shaped abrasive discs, model convex blocks matched with the size and the shape of the abrasive discs are arranged on the bottom surface of the third disc body, and the abrasive discs are fixed on the model convex blocks, so that the abrasive disc and the adsorption holes have a height difference, and debris and powder are favorably adsorbed by the adsorption holes, and the abrasive disc is used for polishing the surface of a workpiece;
the grinding material discs of different models are respectively arranged on the first disc body and the third disc body, the grinding material disc of the first model is arranged on the first disc body, the grinding material disc of the second model is arranged on the third disc body, during assembly, the sliding connector is clamped in the groove disc connecting pipe in a sliding mode, the first disc body is located in the second fan-shaped holes, the bottom surface of the first disc body and the bottom surface of the third disc body are located on different horizontal planes, each second disc body is correspondingly attached to the third disc body and located between the two fan-shaped lugs, each fan-shaped lug is correspondingly and movably embedded into each first fan-shaped hole, the top surface of each fan-shaped lug is higher than the top surface of the second disc body, during operation, the rotary driving motor drives the driving conical gear to rotate, the driving conical gear drives the driven conical gear to rotate, the driven conical gear drives the rotary groove disc to rotate, the rotary groove disc drives the sliding disc to rotate, and because the bottom surface of the first disc body and the bottom surface of the third disc body are located on different horizontal planes, therefore, when the rotary grooved disc rotates, the abrasive disc on the first disc body or the abrasive disc on the third disc body contacts with the surface of a workpiece to polish the surface of the workpiece, according to the polishing processing sequence, the abrasive disc with the first model on the first disc body polishes the surface of the workpiece, namely the bottom surface of the first disc body is lower than the bottom surface of the third disc body, then the abrasive disc with the second model on the third disc body polishes the surface of the workpiece, at the moment, the pulling cylinder works to drive the first connecting shaft to extend downwards, the first connecting shaft pushes the second connecting shaft to move downwards, the second connecting shaft pushes the sliding disc to move downwards, so that the bottom surface of the third disc body is lower than the bottom surface of the first disc body, and the top surface height of the fan-shaped convex block is not lower than the top surface height of the second disc body, thus, the work of switching the abrasive disc with the first model to the second model is automatically completed, the grinding disc grinding machine is convenient and quick, and after grinding of the grinding disc of the second type is finished, the sliding disc is driven to return by the pulling cylinder through pulling the first connecting shaft and the second connecting shaft, so that the grinding disc of the first type is located at the working position, and the first connecting shaft is connected with the second connecting shaft through the first bearing, so that the sliding disc cannot drive the first connecting shaft to rotate in the rotating process; meanwhile, in the grinding and polishing process, the dust storage chamber is vacuumized through the vacuum suction nozzle, and chips and powder generated by grinding are sucked into the dust storage chamber through the adsorption holes in a negative pressure state, so that the surface of a workpiece is cleaned, and the influence of the chips and the powder on the polishing effect is avoided;
and to the work piece that need the abrasive material dish of a model can accomplish polishing, the bottom surface height through pulling up the cylinder adjustment third disk body is in same horizontal plane with the bottom surface height of first disk body to the abrasive material dish of installation the same model is polished workpiece surface, thereby can improve polishing's efficiency, and the structure is nimble.
CN201910938403.3A 2019-09-30 2019-09-30 Polishing method Active CN110640632B (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN201910938403.3A CN110640632B (en) 2019-09-30 2019-09-30 Polishing method

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN201910938403.3A CN110640632B (en) 2019-09-30 2019-09-30 Polishing method

Publications (2)

Publication Number Publication Date
CN110640632A CN110640632A (en) 2020-01-03
CN110640632B true CN110640632B (en) 2021-12-28

Family

ID=68993395

Family Applications (1)

Application Number Title Priority Date Filing Date
CN201910938403.3A Active CN110640632B (en) 2019-09-30 2019-09-30 Polishing method

Country Status (1)

Country Link
CN (1) CN110640632B (en)

Families Citing this family (2)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN115106949B (en) * 2021-03-17 2023-07-28 广东博智林机器人有限公司 Polishing assembly and polishing robot
CN118650534B (en) * 2024-08-19 2025-02-25 扬州通航汽车配件有限公司 A metal material grinding and polishing machine for automobile parts production

Citations (6)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
GB9313632D0 (en) * 1993-07-01 1993-08-18 Black & Decker Inc Improvements in or relating to flange locks
CN105484755A (en) * 2015-12-22 2016-04-13 中国铁建重工集团有限公司 Cutter disc of shield tunneling machine and shield tunneling machine
CN206780002U (en) * 2017-03-14 2017-12-22 东莞吉鑫五金科技有限公司 Quick tool change system for CNC milling center
CN207642928U (en) * 2017-12-28 2018-07-24 深圳磨霸智能科技有限公司 A kind of belt wheel transmission mechanism for sanding and polishing and mirror finish lathe
WO2019046973A1 (en) * 2017-09-11 2019-03-14 Dean Mayerle Weed seed destruction
CN209190514U (en) * 2018-12-06 2019-08-02 台州扬天建设有限公司 A kind of mill component of sanding machine

Patent Citations (6)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
GB9313632D0 (en) * 1993-07-01 1993-08-18 Black & Decker Inc Improvements in or relating to flange locks
CN105484755A (en) * 2015-12-22 2016-04-13 中国铁建重工集团有限公司 Cutter disc of shield tunneling machine and shield tunneling machine
CN206780002U (en) * 2017-03-14 2017-12-22 东莞吉鑫五金科技有限公司 Quick tool change system for CNC milling center
WO2019046973A1 (en) * 2017-09-11 2019-03-14 Dean Mayerle Weed seed destruction
CN207642928U (en) * 2017-12-28 2018-07-24 深圳磨霸智能科技有限公司 A kind of belt wheel transmission mechanism for sanding and polishing and mirror finish lathe
CN209190514U (en) * 2018-12-06 2019-08-02 台州扬天建设有限公司 A kind of mill component of sanding machine

Also Published As

Publication number Publication date
CN110640632A (en) 2020-01-03

Similar Documents

Publication Publication Date Title
CN110722448B (en) Polishing mechanism capable of automatically replacing abrasive disc in lifting mode
CN110788722B (en) Polishing machine and polishing method for automatic tool change
CN110682199B (en) A polishing mechanism that realizes diameter reduction through plane thread expansion shaft
CN111185832B (en) Aluminium alloy surface cleaning device based on internet
CN212420727U (en) Part grinding device for machining
CN110640596B (en) Polishing mechanism capable of realizing rough and fine polishing integration and polishing method
CN110666651B (en) A polishing machine with automatic tool change
CN110625507B (en) A polishing disc and polishing method for realizing variable diameter by lever
CN112935963A (en) Decorative board grinding device for furniture design
CN221270544U (en) Shock absorber aluminum pipe inner wall grinding device
CN211277886U (en) Polishing mechanism capable of automatically replacing abrasive disc in lifting mode
CN110712104B (en) Can realize automatic equipment of polishing of changing three kinds of model abrasive material discs
KR101370532B1 (en) Polishing apparatus of discharge valve for reciprocating compressor
CN110666666B (en) Polishing equipment for realizing reducing through gear and rack matching
CN207757362U (en) A kind of auto parts and components grinding device
CN110722436B (en) Polishing method of reducing polishing manipulator complete machine
CN112192353A (en) Polishing method of polishing robot for realizing diameter change through lever
CN211277885U (en) Polishing mechanism capable of realizing reducing through plane thread expansion shaft
CN110640632A (en) a polishing method
CN110757268B (en) Stainless steel non-stick pan manufacturing, forming and finish machining treatment equipment
CN211220140U (en) Automatic burnishing machine of tool changing
CN115163480B (en) High-precision fracturing pump valve seat and preparation process thereof
CN110695823A (en) A polishing and grinding machine that realizes variable diameter by cooperating with screw and bevel gear
CN210849676U (en) Polishing equipment for realizing reducing through gear and rack matching
CN212886709U (en) High-efficiency sand mill for processing and producing ceramic outer surface

Legal Events

Date Code Title Description
PB01 Publication
PB01 Publication
SE01 Entry into force of request for substantive examination
GR01 Patent grant
GR01 Patent grant
TR01 Transfer of patent right

Effective date of registration: 20230413

Address after: 314000 No. 1773, Huayu Road, Jiaxing Economic and Technological Development Zone, Zhejiang Province

Patentee after: Zhejiang rock Photoelectric Technology Co.,Ltd.

Address before: Room 712, 525 Chuangxin Road, Zhonghe street, Yinzhou District, Ningbo City, Zhejiang Province 315000

Patentee before: Jinghailianke (Ningbo) Intelligent Equipment Co.,Ltd.

TR01 Transfer of patent right
CP03 Change of name, title or address

Address after: 314000 Zhejiang Province Jiaxing City Economic and Technological Development Zone Tanghui Street Huayu Road 1777.NO

Patentee after: ZHEJIANG LUOKE PHOTOELECTRIC TECHNOLOGY Co.,Ltd.

Country or region after: China

Address before: 314000 No. 1773, Huayu Road, Jiaxing Economic and Technological Development Zone, Zhejiang Province

Patentee before: Zhejiang rock Photoelectric Technology Co.,Ltd.

Country or region before: China

CP03 Change of name, title or address