CN110509018B - Workpiece transferring and press-fitting device - Google Patents
Workpiece transferring and press-fitting device Download PDFInfo
- Publication number
- CN110509018B CN110509018B CN201910621494.8A CN201910621494A CN110509018B CN 110509018 B CN110509018 B CN 110509018B CN 201910621494 A CN201910621494 A CN 201910621494A CN 110509018 B CN110509018 B CN 110509018B
- Authority
- CN
- China
- Prior art keywords
- bracket
- horizontally
- plate
- fixed
- workpiece
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P19/00—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes
- B23P19/001—Article feeders for assembling machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P19/00—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes
- B23P19/001—Article feeders for assembling machines
- B23P19/007—Picking-up and placing mechanisms
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23P—METAL-WORKING NOT OTHERWISE PROVIDED FOR; COMBINED OPERATIONS; UNIVERSAL MACHINE TOOLS
- B23P19/00—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes
- B23P19/02—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes for connecting objects by press fit or for detaching same
- B23P19/027—Machines for simply fitting together or separating metal parts or objects, or metal and non-metal parts, whether or not involving some deformation; Tools or devices therefor so far as not provided for in other classes for connecting objects by press fit or for detaching same using hydraulic or pneumatic means
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Automatic Assembly (AREA)
- Press Drives And Press Lines (AREA)
Abstract
Description
技术领域technical field
本发明属于工件加工机械设备领域,尤其涉及一种工件移送压装装置,主要应用于工件的组装加工。The invention belongs to the field of workpiece processing machinery and equipment, and in particular relates to a workpiece transfer and pressing device, which is mainly applied to the assembly and processing of workpieces.
背景技术Background technique
机械工件是组成机械和机械不可分拆的单个制件,它在自动化工业中起着重要的作用,机械工件包括零部件的联接,起支承作用的零部件,起润滑作用的润滑系统和密封零部件,传递运动和能量的传动系统的零部件,在对机械工件进行生产加工的过程中,工件在依次经过压铸成型、磨砂加工和打孔加工等加工步骤后,需要将单独加工完成的工件进行组装,将两个工件组装成一个组合的工件,使得组装在一起的工件能被后道工序或大型设备便捷的使用,现有的机械自动装配是指按照设计的技术要求实现机械工件或部件的连接,把机械工件或部件组合成组合工件,机械装配是机器制造和修理的重要环节,特别是对机械制造来说,高效的机械组装能够大大提高设备装备的效率,还能提高工件组装和设备装配的质量。机械装配是机械制造中最后决定机械产品质量的重要工艺过程,即使是全部合格的工件,如果组装不当,往往也不能形成质量合格的产品,简单的产品可由工件直接装配而成,复杂的产品则须先将若干工件装配成部件,称为部件装配;然后将若干部件和另外一些工件装配成完整的产品,称为总装配。现有的工件组装方法是人工手动协助组装设备将工件进行组装,在工件的整个组装过程中,需要人工手动将工件逐个放置到组装设备上进行组装,工件的组装效率较低,难以满足大批量的工业化生产需要,并且在工件的整个组装过程中,工人的劳动强度较大,工人在将工件连续取放的过程中,由于工人的误操作和连续生产加工的疲惫,还容易被组装设备夹伤,造成工人的生产安全事故。现有的工件组装难以高效平稳的实现组装加工,工件组装加工的效率和质量难以得到保证,并且工件组装加工的自动化程度低,不能满足加工使用的需要。The mechanical workpiece is a single inseparable piece of machinery and machinery, which plays an important role in the automation industry. The mechanical workpiece includes the connection of parts, the parts that play a supporting role, the lubrication system that plays the role of lubrication and the sealing parts. Parts, parts of the transmission system that transmit motion and energy, in the process of producing and processing mechanical workpieces, after the workpieces have undergone processing steps such as die-casting, sanding, and drilling in sequence, the individually processed workpieces need to be processed. Assembling, assembling two workpieces into a combined workpiece, so that the assembled workpiece can be conveniently used by subsequent processes or large equipment. The existing mechanical automatic assembly refers to the realization of mechanical workpieces or components according to the technical requirements of the design. Connect, combine mechanical workpieces or components into composite workpieces. Mechanical assembly is an important part of machine manufacturing and repair. Especially for machine manufacturing, efficient mechanical assembly can greatly improve the efficiency of equipment and equipment, and can also improve workpiece assembly and equipment. Assembly quality. Mechanical assembly is an important process in machinery manufacturing that finally determines the quality of mechanical products. Even if all qualified workpieces are improperly assembled, they often cannot form qualified products. Simple products can be directly assembled from workpieces, while complex products are Several workpieces must be assembled into components, which is called component assembly; then several components and other workpieces must be assembled into a complete product, which is called general assembly. The existing workpiece assembly method is to manually assist the assembly equipment to assemble the workpieces. During the entire assembly process of the workpieces, the workpieces need to be manually placed on the assembly equipment one by one for assembly. The assembly efficiency of the workpieces is low, and it is difficult to meet the needs of large batches. In addition, during the entire assembly process of the workpiece, the labor intensity of the workers is relatively large. During the process of continuously picking and placing the workpiece, the workers are easily clamped by the assembly equipment due to the misoperation of the workers and the fatigue of continuous production and processing. injury, resulting in a worker's production safety accident. The existing workpiece assembly is difficult to achieve efficient and stable assembly and processing, the efficiency and quality of the workpiece assembly and processing are difficult to be guaranteed, and the automation degree of the workpiece assembly and processing is low, which cannot meet the needs of processing and use.
发明内容SUMMARY OF THE INVENTION
本发明所要解决的技术问题是克服现有技术中所存在的上述不足,而提供一种结构设计合理,可以将工件便捷准确的移送至所需的压装工位,并能够将工件平稳高效的进行压装加工,自动化程度高,满足加工使用需要的工件移送压装装置。The technical problem to be solved by the present invention is to overcome the above-mentioned deficiencies in the prior art, and to provide a kind of reasonable structure design, which can conveniently and accurately transfer the workpiece to the required pressing station, and can move the workpiece smoothly and efficiently. It is a workpiece transfer and press-fitting device that performs press-fitting processing with a high degree of automation and meets the needs of processing and use.
为了解决上述技术问题,本发明所采用的技术方案是:一种工件移送压装装置,其特征在于:所述工件移送压装装置包括工件加工支架、工件移送机构和工件压装机构,所述工件移送机构和工件压装机构沿水平方向依次设置于工件加工支架上侧,所述工件移送机构包括移料链条、移料电机、第一传送带、第二传送带和放料承板,所述工件加工支架下方两侧分别水平固定设置有第一固定承板和第二固定承板,第一固定承板和第二固定承板从下至上依次水平设置,所述第一固定承板上侧水平固定设置有第一传送支架,第一传送支架端部竖直转动连接有第一传送辊,第一传送带水平设置于第一传送支架上侧,第一传送带卷绕连接于第一传送辊,所述第二固定承板上侧水平固定设置有第二传送支架,第二传送支架端部竖直转动连接有第二传送辊,第二传送带水平设置于第二传送支架上侧,第二传送带卷绕连接于第二传送辊,所述工件加工支架上方两侧分别竖直转动连接有移料链轮,所述移料链条水平设置于工件加工支架上方一侧,移料链条两侧分别卷绕连接于工件加工支架两侧的移料链轮,所述移料电机水平固定设置于工件加工支架上方一侧,移料电机输出端竖直设置有主皮带轮,工件加工支架一侧的移料链轮上竖直同轴设置有辅皮带轮,主皮带轮和辅皮带轮之间采用移料皮带传动连接,所述移料链条下方一侧的工件加工支架上水平固定设置有第一移料导杆,移料链条上方另一侧的工件加工支架上水平固定设置有第二移料导杆,所述第一移料导杆上沿水平方向滑动设置有第一移料板,移料链条下侧两端分别与第一移料板两侧固定连接,第一移料板下端水平固定设置有第一连接板,第一连接板一侧水平固定设置有第一气缸,第一气缸与第一传送带相互垂直,第一气缸输出端水平固定设置有第一吸附连板,所述第二移料导杆上沿水平方向滑动设置有第二移料板,移料链条上侧两端分别与第二移料板两侧固定连接,第二移料板下端水平固定设置有第二连接板,第二连接板一侧水平转动连接有翻转转轴,翻转转轴端部水平固定设置有翻转支架,翻转支架内水平固定设置有第二气缸,第二气缸与第二传送带相互垂直,第二气缸输出端水平固定设置有第二吸附连板,所述翻转转轴上竖直固定设置有翻转齿轮,翻转齿轮一侧的工件加工支架上水平固定设置有齿板支架,齿板支架端部水平固定设置有翻转齿板,翻转齿板与移料链条相互平行,所述第一传送带和第二传送带之间的工件加工支架上水平固定设置有承板底座,承板底座上水平固定设置有缓冲底板,所述放料承板水平固定设置于缓冲底板上侧,放料承板水平设置于第一传送带和第二传送带之间,放料承板上侧表面与第一传送带上侧表面处于同一水平位置,所述工件压装机构包括压装支架、转动电机、转动圆盘、环状导板、压杆支架、转动压杆、升降连杆、升降齿条、压装齿轮和压装齿条,所述压装支架水平固定设置于工件加工支架上方一侧,所述转动圆盘水平转动连接于压装支架上侧,转动圆盘下侧中部竖直同轴设置有压装转轴,压装转轴下侧端部水平固定设置有压装辅带轮,所述压装支架下方一侧水平固定设置有电机支架,转动电机竖直向上固定设置于电机支架下侧,转动电机输出端水平设置有压装主带轮,所述压装主带轮和压装辅带轮之间采用压装皮带传动连接,所述转动圆盘上方外侧水平固定设置有环状导板,环状导板上侧表面均匀设置有导杆提升斜面,导杆提升斜面低端和导杆提升斜面高端的连接处设置有阶梯状结构的导杆下落斜面,所述导杆下落斜面和导杆提升斜面的连接转角处均采用圆弧面过渡连接,所述转动圆盘一侧的压装支架上水平固定设置有压杆支架,转动压杆设置于转动圆盘上侧,转动压杆端部铰连接于压杆支架上侧端部,所述压杆支架和转动压杆均沿转动圆盘的径向依次设置,所述压装支架一侧水平固定设置有齿轮支架,压装齿轮竖直转动连接于齿轮支架一侧,压装齿轮两侧分别竖直固定设置有前齿条支架和后齿条支架,所述升降齿条沿竖直方向滑动设置于前齿条支架,压装齿条沿竖直方向滑动设置于后齿条支架,压装齿轮两侧分别与升降齿条和压装齿条啮合连接,所述转动压杆与升降齿条之间设置有升降连杆,升降连杆上下两端分别铰连接于转动压杆端部和升降齿条上端,所述压装齿条下端水平固定设置有升降压板,所述转动压杆下方中部固定设置有滚珠底座,滚珠底座下侧滚动设置有承杆滚珠,承杆滚珠设置于环状导板上侧,所述转动圆盘一侧的压装支架上竖直固定设置有与转动压杆宽度相适配的限位支架,转动压杆设置于限位支架内,所述转动压杆与限位支架之间倾斜设置有压装拉簧。In order to solve the above technical problems, the technical solution adopted in the present invention is: a workpiece transfer and press-fitting device, characterized in that: the workpiece transfer and press-fit device comprises a workpiece processing bracket, a workpiece transfer mechanism and a workpiece press-fit mechanism, the The workpiece transfer mechanism and the workpiece pressing mechanism are sequentially arranged on the upper side of the workpiece processing support along the horizontal direction. A first fixed support plate and a second fixed support plate are respectively horizontally fixed on both sides of the lower part of the processing bracket, the first fixed support plate and the second fixed support plate are arranged horizontally from bottom to top in sequence, and the upper side of the first fixed support plate is horizontal A first transmission bracket is fixedly arranged, the end of the first transmission bracket is vertically rotated and connected with a first transmission roller, the first transmission belt is horizontally arranged on the upper side of the first transmission bracket, and the first transmission belt is wound and connected to the first transmission roller, so A second transmission bracket is horizontally fixed on the upper side of the second fixed support plate, and the end of the second transmission bracket is vertically rotatably connected with a second transmission roller. It is wound around and connected to the second conveying roller, and the upper two sides of the workpiece processing support are respectively connected with moving material sprockets that rotate vertically. The material-moving sprockets are connected to both sides of the workpiece processing support, the material-moving motor is horizontally fixed on the upper side of the workpiece processing support, the output end of the material-moving motor is vertically provided with a main pulley, and the material-moving chain on one side of the workpiece processing support The auxiliary pulley is vertically and coaxially arranged on the wheel, and the main pulley and the auxiliary pulley are connected by a material-moving belt. A second material moving guide rod is horizontally fixed on the workpiece processing bracket on the other side above the material chain, and a first material moving plate is slidably arranged on the first material moving guide rod along the horizontal direction. They are respectively fixedly connected with both sides of the first moving plate, the lower end of the first moving plate is fixed with a first connecting plate horizontally, and one side of the first connecting plate is fixed with a first cylinder horizontally, and the first cylinder and the first conveyor belt are perpendicular to each other , the output end of the first cylinder is fixed with a first adsorption connecting plate horizontally, the second material moving guide rod is slidably provided with a second material moving plate along the horizontal direction, and the two ends of the upper side of the material moving chain are respectively connected with the second material moving plate. The two sides of the plate are fixedly connected, the lower end of the second feeding plate is fixed with a second connecting plate horizontally, one side of the second connecting plate is horizontally connected with a turning shaft, and the end of the turning shaft is horizontally fixed with a turning bracket, and the inside of the turning bracket is horizontally fixed A second air cylinder is arranged, the second air cylinder and the second conveyor belt are perpendicular to each other, the output end of the second air cylinder is fixed with a second adsorption connecting plate horizontally, and a turning gear is vertically fixed on the turning shaft, and the workpiece on one side of the turning gear is fixed vertically. A toothed plate bracket is fixed horizontally on the processing bracket, and a turning toothed plate is fixed horizontally at the end of the toothed plate bracket. The turning toothed plate and the material moving chain are parallel to each other. The workpiece processing bracket between the first conveyor belt and the second conveyor belt A support plate base is fixed horizontally, and a buffer bottom plate is fixed horizontally on the support plate base , the discharge bearing plate is horizontally fixed on the upper side of the buffer bottom plate, the discharge bearing plate is horizontally arranged between the first conveyor belt and the second conveyor belt, and the upper surface of the discharge bearing plate and the upper surface of the first conveyor belt are at the same level position, the workpiece pressing mechanism includes a pressing bracket, a rotating motor, a rotating disc, an annular guide plate, a pressing rod bracket, a rotating pressing rod, a lifting link, a lifting rack, a pressing gear and a pressing rack. The press-fitting support is horizontally fixed on the upper side of the workpiece processing support, the rotating disc is connected to the upper side of the press-fitting support in a horizontal rotation, and a press-fitting rotating shaft is vertically and coaxially arranged in the middle of the lower side of the rotating disc. A press-fitting auxiliary pulley is fixed horizontally at the side end, a motor support is fixed horizontally on the lower side of the press-fitting support, the rotating motor is fixed vertically upward on the lower side of the motor support, and the output end of the rotating motor is horizontally set with a press-fitting The main pulley, the press-fit main pulley and the press-fit auxiliary pulley are connected by a press-fit belt drive, an annular guide plate is fixed horizontally on the upper side of the rotating disc, and the upper surface of the ring-shaped guide plate is evenly provided with The guide rod lifting slope, the connection between the low end of the guide rod lifting slope and the high end of the guide rod lifting slope is provided with a guide rod falling slope with a stepped structure, and the connecting corners of the guide rod falling slope and the guide rod lifting slope are all arcs. Surface transition connection, a pressure rod bracket is fixed horizontally on the press-fitting bracket on one side of the rotating disc, the rotating pressure rod is arranged on the upper side of the rotating disc, and the end of the rotating pressure rod is hingedly connected to the upper end of the pressure rod bracket , the pressing rod bracket and the rotating pressing rod are arranged in turn along the radial direction of the rotating disc, a gear bracket is fixed horizontally on one side of the pressing bracket, and the pressing gear is vertically rotatably connected to one side of the gear bracket. A front rack bracket and a rear rack bracket are vertically fixed on both sides of the gear, the lifting rack is slidably arranged on the front rack bracket along the vertical direction, and the press-fit rack is slidably arranged on the rear rack along the vertical direction The bracket, the two sides of the pressing gear are meshed with the lifting rack and the pressing rack, respectively, and a lifting link is arranged between the rotating pressure rod and the lifting rack, and the upper and lower ends of the lifting link are hingedly connected to the rotating pressure rod. The lower end of the press-fitting rack is fixed with a lifting and pressing plate horizontally, and a ball base is fixed in the lower middle of the rotating pressure rod. On the upper side of the annular guide plate, a limit bracket adapted to the width of the rotating pressure rod is vertically fixed on the press-fitting support on one side of the rotating disc. A pressure-loaded tension spring is inclined between the pressure rod and the limit bracket.
进一步地,所述工件加工支架两侧的第一移料导杆和第二移料导杆均为正多边形结构的长杆。Further, the first material moving guide rod and the second material moving guide rod on both sides of the workpiece processing support are long rods with a regular polygon structure.
进一步地,所述第一吸附连板一侧设置有弧形结构的第一卡槽,第一卡槽内设置有第一电磁铁,所述第二吸附连板一侧设置有弧形结构的第二卡槽,第二卡槽内设置有第二电磁铁。Further, one side of the first adsorption connecting plate is provided with an arc-shaped first clamping slot, a first electromagnet is arranged in the first clamping slot, and one side of the second adsorption connecting plate is provided with an arc-shaped structure. The second card slot is provided with a second electromagnet in the second card slot.
进一步地,所述缓冲底板上侧水平设置有缓冲橡胶层,缓冲橡胶层设置在放料承板与缓冲底板之间。Further, a buffer rubber layer is horizontally arranged on the upper side of the buffer bottom plate, and the buffer rubber layer is arranged between the discharge bearing plate and the buffer bottom plate.
进一步地,所述限位支架内的转动压杆两侧分别对称滚动设置有限位滚珠。Further, limit balls are respectively rolled symmetrically on both sides of the rotating pressure rod in the limit bracket.
进一步地,所述压装齿条下端的升降压板下侧水平固定设置有压装橡胶层。Further, a press-fit rubber layer is fixed horizontally on the lower side of the lifting and pressing plate at the lower end of the press-fit rack.
本发明与现有技术相比,具有以下优点和效果:本发明结构设计合理,通过工件移送机构和工件压装机构沿水平方向依次设置于工件加工支架上侧,利用工件移送机构使能将工件便捷准确的移送至所需的压装工位,利用工件压装机构使能将移送至压装工位的工件平稳高效的进行压装加工,实现工件自动组装,通过第一固定承板和第二固定承板从下至上依次水平设置,第一传送带水平设置于第一传送支架上侧,第二传送带水平设置于第二传送支架上侧,利用第一传送带和第二传送带同步相向进行传送,使能将需要组装加工的两个工件沿水平方向同步相向进行传送,通过移料链条两侧分别卷绕连接于工件加工支架两侧的移料链轮,移料电机输出端的主皮带轮和移料链轮上竖直同轴设置的辅皮带轮之间采用移料皮带传动连接,利用移料电机连续往复带动移料链轮进行转动,使得移料链条能够连续往复进行转动传送,通过第一移料导杆上沿水平方向滑动设置有第一移料板,移料链条下侧两端分别与第一移料板两侧固定连接,第二移料导杆上沿水平方向滑动设置有第二移料板,移料链条上侧两端分别与第二移料板两侧固定连接,第一移料板和第二移料板能够在移料链条的带动下同步相向进行平移运动,利用工件加工支架两侧的第一移料导杆和第二移料导杆均为正多边形结构的长杆,实现第一移料板和第二移料板平稳顺畅的往复平移运动,通过第一移料板下端水平固定设置有第一连接板,第一连接板一侧的第一气缸输出端水平固定设置有第一吸附连板,第二移料板下端水平固定设置有第二连接板,第二连接板一侧的翻转转轴端部水平固定设置有翻转支架,翻转支架内的第二气缸输出端水平固定设置有第二吸附连板,利用第一气缸水平推动第一吸附连板,使能利用第一吸附连板将第一传送带上的工件吸附固定,利用第二气缸水平推动第二吸附连板,使能利用第二吸附连板将第二传送带上的工件吸附固定,利用第一移料板和第二移料板的同步相向进行平移运动,使得第一传送带上的工件和第二传送带上的工件能够同步相向的移送至放料承板上侧,利用第一吸附连板一侧设置有弧形结构的第一卡槽,第一卡槽内设置有第一电磁铁,第二吸附连板一侧设置有弧形结构的第二卡槽,第二卡槽内设置有第二电磁铁,确保第一传送带和第二传送带上的工件能够分别被高效平稳的吸附固定进行平移运动,利用翻转转轴上竖直固定设置有翻转齿轮,工件加工支架的齿板支架端部水平固定设置有翻转齿板,翻转齿板与移料链条相互平行,使得第二移料板在带动翻转支架进行平移的过程中,翻转齿轮能够在翻转齿板的带动下进行转动,实现第二气缸所吸附固定工件的平稳翻转,使得两个工件能够准确的调整至所需的压装工位进行高效压装加工,通过第一传送带和第二传送带之间的工件加工支架上水平固定设置有承板底座,承板底座上水平固定设置有缓冲底板,放料承板水平固定设置于缓冲底板上侧,使能利用放料承板对工件进行支承固定,实现工件高效平稳的压装加工,利用缓冲底板上侧水平设置有缓冲橡胶层,使能对工件在压装加工过程中高效进行缓冲,实现工件平稳有序的压装加工,通过转动圆盘水平转动连接于压装支架上侧,转动圆盘下侧中部竖直同轴设置有压装转轴,转动电机输出端的压装主带轮和压装转轴下侧端部的压装辅带轮之间采用压装皮带传动连接,使得转动圆盘能够在转动电机的带动下连续平稳的转动,利用转动圆盘上方外侧水平固定设置有环状导板,转动圆盘在转动过程中能够带动环状导板同步进行转动,通过转动圆盘一侧的压装支架上水平固定设置有压杆支架,转动压杆端部铰连接于压杆支架上侧端部,转动压杆下方中部的滚珠底座上滚动设置有承杆滚珠,承杆滚珠设置于环状导板上侧,转动圆盘一侧的压装支架上竖直固定设置有与转动压杆宽度相适配的限位支架,转动压杆与限位支架之间倾斜设置有压装拉簧,利用压装拉簧沿倾斜方向向下拉动转动压杆,使得转动压杆下方的承杆滚珠能够紧密的压紧于环状导板表面,承杆滚珠能够在环状导板的转动过程中沿着环状导板表面顺畅的进行滚动,通过环状导板上侧表面均匀设置有导杆提升斜面,导杆提升斜面低端和导杆提升斜面高端的连接处设置有阶梯状结构的导杆下落斜面,导杆下落斜面和导杆提升斜面的连接转角处均采用圆弧面过渡连接,使得环状导板在转动过程中能够利用导杆提升斜面和导杆下落斜面带动转动压杆往复进行摆动,并能实现转动压杆端部缓慢摆动提升和快速摆动下落,利用转动压杆设置于限位支架内,使能实现转动压杆平稳准确的往复摆动,避免转动压杆在摆动过程中产生偏移歪斜,利用限位支架内的转动压杆两侧分别对称滚动设置有限位滚珠,使得转动压杆在往复摆动过程中能够利用限位滚珠沿着限位支架内侧高效顺畅的往复摆动,实现转动压杆高效平稳的连续摆动,通过压装齿轮竖直转动连接于齿轮支架一侧,压装齿轮两侧分别竖直固定设置有前齿条支架和后齿条支架,升降齿条沿竖直方向滑动设置于前齿条支架,压装齿条沿竖直方向滑动设置于后齿条支架,转动压杆与升降齿条之间设置有升降连杆,利用转动圆盘带动转动压杆沿竖直方向往复进行摆动,转动压杆能够利用升降连杆带动升降齿条进行升降运动,利用压装齿轮两侧分别与升降齿条和压装齿条啮合连接,使得压装齿条能够与升降齿条同步相向进行升降运动,利用转动压杆端部在导杆提升斜面和导杆下落斜面的作用下能够实现缓慢摆动提升和快速摆动下落,使得压装齿条能够实现缓慢下落和快速提升,利用压装齿条下端水平固定设置有升降压板,当升降压板在压装齿条的带动下缓慢下落的过程中,能够平缓均匀的将工件进行压装加工,避免工件在压装加工过程中产生歪斜误差,提高工件压装加工的质量,当升降压板在压装齿条的带动下快速提升的过程中,使得升降压板能够快速高效的与工件表面脱离,使得压装加工完成的工件能够快速取离,并能继续为下一工件的压装加工做好准备,实现工件的连续高效压装加工,利用压装齿条下端的升降压板下侧水平固定设置有压装橡胶层,确保升降压板能够平稳的将工件进行压装加工,通过这样的结构,本发明结构设计合理,可以将工件便捷准确的移送至所需的压装工位,并能够将工件平稳高效的进行压装加工,自动化程度高,满足加工使用的需要。Compared with the prior art, the present invention has the following advantages and effects: the structure of the present invention is reasonable in design, the workpiece transfer mechanism and the workpiece pressing mechanism are sequentially arranged on the upper side of the workpiece processing support along the horizontal direction, and the workpiece transfer mechanism is used to enable the workpiece to be It is convenient and accurate to transfer to the required press-fitting station, and the workpiece press-fitting mechanism enables smooth and efficient press-fitting processing of the workpiece transferred to the press-fitting station, and realizes the automatic assembly of the workpiece. The two fixed support plates are arranged horizontally from bottom to top, the first conveyor belt is horizontally arranged on the upper side of the first transmission bracket, the second conveyor belt is horizontally arranged on the upper side of the second transmission bracket, and the first conveyor belt and the second conveyor belt are used for synchronous transmission in opposite directions. The two workpieces that need to be assembled and processed can be conveyed synchronously and oppositely in the horizontal direction, and the material-moving sprockets connected to the two sides of the workpiece processing bracket are respectively wound on both sides of the material-moving chain, and the main pulley and the material-moving material at the output of the material-moving motor The auxiliary pulleys arranged vertically and coaxially on the sprocket are connected by a material-moving belt, and the material-moving sprocket is continuously reciprocated by the material-moving motor to rotate, so that the material-moving chain can be continuously reciprocated for rotation and transmission. A first moving plate is installed on the guide rod along the horizontal direction, both ends of the lower side of the moving chain are fixedly connected to both sides of the first moving plate, and a second moving guide is installed on the second moving guide rod along the horizontal direction. The upper and both ends of the moving chain are fixedly connected to the two sides of the second moving plate. The first moving plate and the second moving plate can be driven by the moving chain. The first moving guide rod and the second moving guide rod on both sides of the bracket are long rods with regular polygon structure, which realize the smooth and smooth reciprocating translation movement of the first moving plate and the second moving plate. A first connecting plate is fixed horizontally at the lower end of the plate, a first suction connecting plate is fixed horizontally at the output end of the first cylinder on one side of the first connecting plate, and a second connecting plate is fixed horizontally at the lower end of the second moving plate. A turning bracket is fixed horizontally at the end of the turning shaft on one side of the connecting plate, and a second suction connecting plate is fixed horizontally at the output end of the second cylinder in the turning frame, and the first suction connecting plate is horizontally pushed by the first cylinder to enable the The first suction connecting plate adsorbs and fixes the workpiece on the first conveyor belt, and the second suction connecting plate is used to push the second suction connecting plate horizontally, so that the workpiece on the second conveyor belt can be adsorbed and fixed by the second suction connecting plate, and the first moving material is used The synchronous movement of the plate and the second moving plate enables the workpieces on the first conveyor belt and the workpieces on the second conveyor belt to be moved to the upper side of the unloading support plate synchronously. There is a first card slot with an arc-shaped structure, a first electromagnet is arranged in the first card slot, a second card slot with an arc-shaped structure is arranged on one side of the second adsorption connecting plate, and a second electromagnet is arranged in the second card slot. Iron, to ensure that the workpieces on the first conveyor belt and the second conveyor belt can be respectively adsorbed and fixed efficiently and smoothly for translational movement, and a flipping gear is fixed vertically on the flipping shaft, and the end of the tooth plate bracket of the workpiece processing bracket is fixed horizontally. Turn the toothed plate, the turning toothed plate and the moving chain are parallel to each other, so that the second moving plate is driving the turning During the translation process of the bracket, the overturning gear can rotate under the drive of the overturning tooth plate, so as to realize the smooth overturning of the fixed workpiece adsorbed by the second cylinder, so that the two workpieces can be accurately adjusted to the required pressing station for high efficiency. For press-fitting processing, a support plate base is fixed horizontally on the workpiece processing bracket between the first conveyor belt and the second conveyor belt, a buffer base plate is fixed horizontally on the base plate, and the discharge support plate is fixed horizontally on the upper side of the buffer base plate. , so that the workpiece can be supported and fixed by the unloading support plate, and the efficient and stable press-fitting processing of the workpiece can be realized. The buffer rubber layer is horizontally arranged on the upper side of the buffer bottom plate, so that the workpiece can be efficiently buffered during the press-fitting process. The workpiece is press-fitted in a stable and orderly manner. It is connected to the upper side of the press-fit bracket by rotating the disc horizontally. The middle of the lower side of the rotary disc is provided with a press-fit shaft vertically and coaxially. The press-fitting auxiliary pulleys at the lower end of the rotating shaft are connected by press-fitting belt transmission, so that the rotating disc can rotate continuously and smoothly under the drive of the rotating motor. , the rotating disc can drive the ring-shaped guide plate to rotate synchronously during the rotation process, a pressure rod bracket is fixed horizontally on the press-fitting bracket on one side of the rotating disc, and the end of the rotating pressure rod is hinged to the upper end of the pressure rod bracket The ball base in the middle of the lower part of the rotating pressure rod is rolled with bearing rod balls, and the bearing rod balls are arranged on the upper side of the ring-shaped guide plate. The suitable limit bracket, the pressure-loading tension spring is inclined between the rotating pressure rod and the limit bracket, and the pressure-loading tension spring is used to pull the rotating pressure rod downward in the inclined direction, so that the bearing rod ball under the rotating pressure rod can be tightly It is pressed against the surface of the ring-shaped guide plate, and the ball bearing rod can roll smoothly along the surface of the ring-shaped guide plate during the rotation of the ring-shaped guide plate. The connection between the lower end of the slope and the upper end of the guide rod lifting slope is provided with a guide rod falling slope with a stepped structure, and the connecting corners of the guide rod falling slope and the guide rod lifting slope are all connected by a circular arc surface transition connection, so that the annular guide plate rotates During the process, the lifting slope of the guide rod and the falling slope of the guide rod can be used to drive the rotating pressure rod to swing back and forth, and the end of the rotating pressure rod can be slowly swayed to lift and quickly swayed to fall. The rotating pressure rod is set in the limit bracket to enable Realize the stable and accurate reciprocating swing of the rotating pressure rod, avoid the offset and skew of the rotating pressure rod during the swinging process, and use the two sides of the rotating pressure rod in the limit bracket to roll symmetrically to set the limit balls, so that the rotating pressure rod can be in the reciprocating swing process. The limit ball can be used to swing back and forth efficiently and smoothly along the inner side of the limit bracket, so as to realize the efficient and stable continuous swing of the rotating pressure rod. A front rack bracket and a rear rack bracket are fixedly arranged, the lifting rack is slidably arranged on the front rack bracket along the vertical direction, the press-fit rack is slidably arranged on the rear rack bracket along the vertical direction, and the rotating pressure rod and the lifting gear set between bars with The lifting link uses the rotating disc to drive the rotating pressure rod to reciprocate in the vertical direction. The rotating pressure rod can use the lifting link to drive the lifting rack to move up and down. The two sides of the pressing gear are used to connect with the lifting rack and the pressing rod respectively. The rack is meshed and connected, so that the pressing rack can move up and down synchronously with the lifting rack, and the end of the rotating pressure rod can achieve slow swing lifting and fast swing falling under the action of the guide rod lifting slope and the guide rod falling slope. The press-fit rack can achieve slow falling and rapid lifting. The lower end of the press-fit rack is horizontally fixed with a lifting and pressing plate. When the lifting and pressing plate is slowly falling under the drive of the press-fitting rack, the workpiece can be smoothly and evenly moved. Press-fit processing can avoid skew error of the workpiece during the press-fit process, and improve the quality of the workpiece press-fit process. When the lifting and pressing plate is rapidly lifted under the drive of the pressing rack, the lifting and pressing plate can be quickly and efficiently connected to the workpiece. The surface is separated, so that the workpiece after the press-fitting process can be quickly removed, and can continue to prepare for the press-fitting processing of the next workpiece, so as to realize the continuous and efficient press-fitting processing of the workpiece. A press-fitting rubber layer is fixed horizontally to ensure that the lifting and pressing plate can smoothly press-fit the workpiece. Through such a structure, the present invention has a reasonable structure design, and the workpiece can be conveniently and accurately transferred to the required press-fitting station. It can press-fit the workpiece smoothly and efficiently, with a high degree of automation, meeting the needs of processing and use.
附图说明Description of drawings
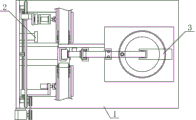
图1是本发明一种工件移送压装装置的主视结构示意图。FIG. 1 is a schematic view of the front structure of a workpiece transferring and pressing device according to the present invention.
图2是本发明一种工件移送压装装置的俯视结构示意图。FIG. 2 is a schematic top view of the structure of a workpiece transferring and pressing device according to the present invention.
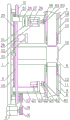
图3是本发明的工件移送机构的右视结构示意图。FIG. 3 is a schematic view of the right side view of the workpiece transfer mechanism of the present invention.
图4是本发明的工件移送机构的俯视结构示意图。FIG. 4 is a schematic plan view of the workpiece transfer mechanism of the present invention.
图5是本发明的工件压装机构的主视结构示意图。FIG. 5 is a schematic front view of the structure of the workpiece pressing mechanism of the present invention.
图6是本发明的工件压装机构的俯视结构示意图。6 is a schematic top view of the structure of the workpiece pressing mechanism of the present invention.
图中:1.工件加工支架,2.工件移送机构,3.工件压装机构,4.移料链条,5.移料电机,6.第一传送带,7.第二传送带,8.放料承板,9.第一固定承板,10.第二固定承板,11.第一传送支架,12.第一传送辊,13.第二传送支架,14.第二传送辊,15.移料链轮,16.主皮带轮,17.辅皮带轮,18.移料皮带,19.第一移料导杆,20.第二移料导杆,21.第一移料板,22.第一连接板,23.第一气缸,24.第一吸附连板,25.第二移料板,26.第二连接板,27.翻转转轴,28.翻转支架,29.第二气缸,30.第二吸附连板,31.翻转齿轮,32.齿板支架,33.翻转齿板,34.承板底座,35.缓冲底板,36.压装支架,37.转动电机,38.转动圆盘,39.环状导板,40.压杆支架,41.转动压杆,42.升降连杆,43.升降齿条,44.压装齿轮,45.压装齿条,46.压装转轴,47.压装辅带轮,48.电机支架,49.压装主带轮,50.压装皮带,51.导杆提升斜面,52.导杆下落斜面,53.齿轮支架,54.前齿条支架,55.后齿条支架,56.升降压板,57.滚珠底座,58.承杆滚珠,59.限位支架,60.压装拉簧,61.第一卡槽,62.第一电磁铁,63.第二卡槽,64.第二电磁铁,65.缓冲橡胶层,66.限位滚珠,67.压装橡胶层。In the picture: 1. Workpiece processing support, 2. Workpiece transfer mechanism, 3. Workpiece pressing mechanism, 4. Material moving chain, 5. Material moving motor, 6. The first conveyor belt, 7. The second conveyor belt, 8. The discharge bearing plate, 9. first fixed bearing plate, 10. second fixed bearing plate, 11. first conveying support, 12. first conveying roller, 13. second conveying support, 14. second conveying roller, 15. shift Material sprocket, 16. Main pulley, 17. Auxiliary pulley, 18. Material transfer belt, 19. First material transfer guide rod, 20. Second material transfer guide rod, 21. First material transfer plate, 22. First material Connecting plate, 23. First air cylinder, 24. First suction connecting plate, 25. Second feeding plate, 26. Second connecting plate, 27. Turning shaft, 28. Turning bracket, 29. Second air cylinder, 30. The second adsorption connecting plate, 31. Turning gear, 32. Tooth plate bracket, 33. Turning tooth plate, 34. Support plate base, 35. Buffer bottom plate, 36. Press-fit bracket, 37. Rotating motor, 38. Rotating disc , 39. Ring-shaped guide plate, 40. Pressure rod bracket, 41. Rotating pressure rod, 42. Lifting link, 43. Lifting rack, 44. Press-fit gear, 45. Press-fit rack, 46. Press-fit shaft, 47. Press-fit auxiliary pulley, 48. Motor bracket, 49. Press-fit main pulley, 50. Press-fit belt, 51. Guide rod lifting ramp, 52. Guide rod falling ramp, 53. Gear bracket, 54. Front teeth Rack bracket, 55. Rear rack bracket, 56. Lifting and pressing plate, 57. Ball base, 58. Bearing rod ball, 59. Limit bracket, 60. Press-fit tension spring, 61. First slot, 62. First Electromagnet, 63. Second slot, 64. Second electromagnet, 65. Buffer rubber layer, 66. Limit ball, 67. Press-fit rubber layer.
具体实施方式Detailed ways
为了进一步描述本发明,下面结合附图进一步阐述一种工件移送压装装置的具体实施方式,以下实施例是对本发明的解释而本发明并不局限于以下实施例。In order to further describe the present invention, a specific embodiment of a workpiece transfer and press-fitting device is further described below with reference to the accompanying drawings. The following examples are for explaining the present invention and the present invention is not limited to the following examples.
如图1和图2所示,本发明一种工件移送压装装置,包括工件加工支架1、工件移送机构2和工件压装机构3,工件移送机构2和工件压装机构3沿水平方向依次设置于工件加工支架1上侧,如图3和图4所示,本发明的工件移送机构2包括移料链条4、移料电机5、第一传送带6、第二传送带7和放料承板8,工件加工支架1下方两侧分别水平固定设置有第一固定承板9和第二固定承板10,第一固定承板9和第二固定承板10从下至上依次水平设置,第一固定承板9上侧水平固定设置有第一传送支架11,第一传送支架11端部竖直转动连接有第一传送辊12,第一传送带6水平设置于第一传送支架11上侧,第一传送带6卷绕连接于第一传送辊12,第二固定承板10上侧水平固定设置有第二传送支架13,第二传送支架13端部竖直转动连接有第二传送辊14,第二传送带7水平设置于第二传送支架13上侧,第二传送带7卷绕连接于第二传送辊14,工件加工支架1上方两侧分别竖直转动连接有移料链轮15,移料链条4水平设置于工件加工支架1上方一侧,移料链条4两侧分别卷绕连接于工件加工支架1两侧的移料链轮15,移料电机5水平固定设置于工件加工支架1上方一侧,移料电机5输出端竖直设置有主皮带轮16,工件加工支架1一侧的移料链轮15上竖直同轴设置有辅皮带轮17,主皮带轮16和辅皮带轮17之间采用移料皮带18传动连接,移料链条4下方一侧的工件加工支架1上水平固定设置有第一移料导杆19,移料链条4上方另一侧的工件加工支架1上水平固定设置有第二移料导杆20,第一移料导杆19上沿水平方向滑动设置有第一移料板21,移料链条4下侧两端分别与第一移料板21两侧固定连接,第一移料板21下端水平固定设置有第一连接板22,第一连接板22一侧水平固定设置有第一气缸23,第一气缸23与第一传送带6相互垂直,第一气缸23输出端水平固定设置有第一吸附连板24,第二移料导杆20上沿水平方向滑动设置有第二移料板25,移料链条4上侧两端分别与第二移料板25两侧固定连接,第二移料板25下端水平固定设置有第二连接板26,第二连接板26一侧水平转动连接有翻转转轴27,翻转转轴27端部水平固定设置有翻转支架28,翻转支架28内水平固定设置有第二气缸29,第二气缸29与第二传送带7相互垂直,第二气缸29输出端水平固定设置有第二吸附连板30,翻转转轴27上竖直固定设置有翻转齿轮31,翻转齿轮31一侧的工件加工支架1上水平固定设置有齿板支架32,齿板支架32端部水平固定设置有翻转齿板33,翻转齿板33与移料链条4相互平行,本发明的第一传送带6和第二传送带7之间的工件加工支架1上水平固定设置有承板底座34,承板底座34上水平固定设置有缓冲底板35,放料承板8水平固定设置于缓冲底板35上侧,放料承板8水平设置于第一传送带6和第二传送带7之间,放料承板8上侧表面与第一传送带6上侧表面处于同一水平位置。如图5和图6所示,本发明的工件压装机构3包括压装支架36、转动电机37、转动圆盘38、环状导板39、压杆支架40、转动压杆41、升降连杆42、升降齿条43、压装齿轮44和压装齿条45,压装支架36水平固定设置于工件加工支架1上方一侧,转动圆盘38水平转动连接于压装支架36上侧,转动圆盘38下侧中部竖直同轴设置有压装转轴46,压装转轴46下侧端部水平固定设置有压装辅带轮47,压装支架36下方一侧水平固定设置有电机支架48,转动电机37竖直向上固定设置于电机支架48下侧,转动电机37输出端水平设置有压装主带轮49,压装主带轮49和压装辅带轮47之间采用压装皮带50传动连接,转动圆盘38上方外侧水平固定设置有环状导板39,环状导板39上侧表面均匀设置有导杆提升斜面51,导杆提升斜面51低端和导杆提升斜面51高端的连接处设置有阶梯状结构的导杆下落斜面52,导杆下落斜面52和导杆提升斜面51的连接转角处均采用圆弧面过渡连接,转动圆盘38一侧的压装支架36上水平固定设置有压杆支架40,转动压杆41设置于转动圆盘38上侧,转动压杆41端部铰连接于压杆支架40上侧端部,压杆支架40和转动压杆41均沿转动圆盘38的径向依次设置,压装支架36一侧水平固定设置有齿轮支架53,压装齿轮44竖直转动连接于齿轮支架53一侧,压装齿轮44两侧分别竖直固定设置有前齿条支架54和后齿条支架55,升降齿条43沿竖直方向滑动设置于前齿条支架54,压装齿条45沿竖直方向滑动设置于后齿条支架55,压装齿轮44两侧分别与升降齿条43和压装齿条45啮合连接,转动压杆41与升降齿条43之间设置有升降连杆42,升降连杆42上下两端分别铰连接于转动压杆41端部和升降齿条43上端,压装齿条45下端水平固定设置有升降压板56,本发明的转动压杆41下方中部固定设置有滚珠底座57,滚珠底座57下侧滚动设置有承杆滚珠58,承杆滚珠58设置于环状导板39上侧,转动圆盘38一侧的压装支架36上竖直固定设置有与转动压杆41宽度相适配的限位支架59,转动压杆41设置于限位支架59内,转动压杆41与限位支架59之间倾斜设置有压装拉簧60。As shown in Figures 1 and 2, a workpiece transfer and press-fitting device of the present invention includes a
本发明的工件加工支架1两侧的第一移料导杆19和第二移料导杆20均为正多边形结构的长杆,实现第一移料板21和第二移料板25平稳顺畅的往复平移运动。本发明的第一吸附连板24一侧设置有弧形结构的第一卡槽61,第一卡槽61内设置有第一电磁铁62,第二吸附连板30一侧设置有弧形结构的第二卡槽63,第二卡槽63内设置有第二电磁铁64,确保第一传送带6和第二传送带7上的工件能够分别被高效平稳的吸附固定进行平移运动。本发明的缓冲底板35上侧水平设置有缓冲橡胶层65,缓冲橡胶层65设置在放料承板8与缓冲底板35之间,使能对工件在压装加工过程中高效进行缓冲,实现工件平稳有序的压装加工。本发明的限位支架59内的转动压杆41两侧分别对称滚动设置有限位滚珠66,使得转动压杆41在往复摆动过程中能够利用限位滚珠66沿着限位支架59内侧高效顺畅的往复摆动,实现转动压杆41高效平稳的连续摆动。本发明的压装齿条45下端的升降压板56下侧水平固定设置有压装橡胶层67,确保升降压板56能够平稳的将工件进行压装加工。The first material moving
采用上述技术方案,本发明一种工件移送压装装置在使用的时候,通过工件移送机构2和工件压装机构3沿水平方向依次设置于工件加工支架1上侧,利用工件移送机构2使能将工件便捷准确的移送至所需的压装工位,利用工件压装机构3使能将移送至压装工位的工件平稳高效的进行压装加工,实现工件自动组装,通过第一固定承板9和第二固定承板10从下至上依次水平设置,第一传送带6水平设置于第一传送支架11上侧,第二传送带7水平设置于第二传送支架13上侧,利用第一传送带6和第二传送带7同步相向进行传送,使能将需要组装加工的两个工件沿水平方向同步相向进行传送,通过移料链条4两侧分别卷绕连接于工件加工支架1两侧的移料链轮15,移料电机5输出端的主皮带轮16和移料链轮15上竖直同轴设置的辅皮带轮17之间采用移料皮带18传动连接,利用移料电机5连续往复带动移料链轮15进行转动,使得移料链条4能够连续往复进行转动传送,通过第一移料导杆19上沿水平方向滑动设置有第一移料板21,移料链条4下侧两端分别与第一移料板21两侧固定连接,第二移料导杆20上沿水平方向滑动设置有第二移料板25,移料链条4上侧两端分别与第二移料板25两侧固定连接,第一移料板21和第二移料板25能够在移料链条4的带动下同步相向进行平移运动,利用工件加工支架1两侧的第一移料导杆19和第二移料导杆20均为正多边形结构的长杆,实现第一移料板21和第二移料板25平稳顺畅的往复平移运动,通过第一移料板21下端水平固定设置有第一连接板22,第一连接板22一侧的第一气缸23输出端水平固定设置有第一吸附连板24,第二移料板25下端水平固定设置有第二连接板26,第二连接板26一侧的翻转转轴27端部水平固定设置有翻转支架28,翻转支架28内的第二气缸29输出端水平固定设置有第二吸附连板30,利用第一气缸23水平推动第一吸附连板24,使能利用第一吸附连板24将第一传送带6上的工件吸附固定,利用第二气缸29水平推动第二吸附连板30,使能利用第二吸附连板30将第二传送带7上的工件吸附固定,利用第一移料板21和第二移料板25的同步相向进行平移运动,使得第一传送带6上的工件和第二传送带7上的工件能够同步相向的移送至放料承板8上侧,利用第一吸附连板24一侧设置有弧形结构的第一卡槽61,第一卡槽61内设置有第一电磁铁62,第二吸附连板30一侧设置有弧形结构的第二卡槽63,第二卡槽63内设置有第二电磁铁64,确保第一传送带6和第二传送带7上的工件能够分别被高效平稳的吸附固定进行平移运动,利用翻转转轴27上竖直固定设置有翻转齿轮31,工件加工支架1的齿板支架32端部水平固定设置有翻转齿板33,翻转齿板33与移料链条4相互平行,使得第二移料板25在带动翻转支架28进行平移的过程中,翻转齿轮31能够在翻转齿板33的带动下进行转动,实现第二气缸29所吸附固定工件的平稳翻转,使得两个工件能够准确的调整至所需的压装工位进行高效压装加工,通过第一传送带6和第二传送带7之间的工件加工支架1上水平固定设置有承板底座34,承板底座34上水平固定设置有缓冲底板35,放料承板8水平固定设置于缓冲底板35上侧,使能利用放料承板8对工件进行支承固定,实现工件高效平稳的压装加工,利用缓冲底板35上侧水平设置有缓冲橡胶层65,使能对工件在压装加工过程中高效进行缓冲,实现工件平稳有序的压装加工,通过转动圆盘38水平转动连接于压装支架36上侧,转动圆盘38下侧中部竖直同轴设置有压装转轴46,转动电机37输出端的压装主带轮49和压装转轴46下侧端部的压装辅带轮47之间采用压装皮带50传动连接,使得转动圆盘38能够在转动电机37的带动下连续平稳的转动,利用转动圆盘38上方外侧水平固定设置有环状导板39,转动圆盘38在转动过程中能够带动环状导板39同步进行转动,通过转动圆盘38一侧的压装支架36上水平固定设置有压杆支架40,转动压杆41端部铰连接于压杆支架40上侧端部,转动压杆41下方中部的滚珠底座57上滚动设置有承杆滚珠58,承杆滚珠58设置于环状导板39上侧,转动圆盘38一侧的压装支架36上竖直固定设置有与转动压杆41宽度相适配的限位支架59,转动压杆41与限位支架59之间倾斜设置有压装拉簧60,利用压装拉簧60沿倾斜方向向下拉动转动压杆41,使得转动压杆41下方的承杆滚珠58能够紧密的压紧于环状导板39表面,承杆滚珠58能够在环状导板39的转动过程中沿着环状导板39表面顺畅的进行滚动,通过环状导板39上侧表面均匀设置有导杆提升斜面51,导杆提升斜面51低端和导杆提升斜面51高端的连接处设置有阶梯状结构的导杆下落斜面52,导杆下落斜面52和导杆提升斜面51的连接转角处均采用圆弧面过渡连接,使得环状导板39在转动过程中能够利用导杆提升斜面51和导杆下落斜面52带动转动压杆41往复进行摆动,并能实现转动压杆41端部缓慢摆动提升和快速摆动下落,利用转动压杆41设置于限位支架59内,使能实现转动压杆41平稳准确的往复摆动,避免转动压杆41在摆动过程中产生偏移歪斜,利用限位支架59内的转动压杆41两侧分别对称滚动设置有限位滚珠66,使得转动压杆41在往复摆动过程中能够利用限位滚珠66沿着限位支架59内侧高效顺畅的往复摆动,实现转动压杆41高效平稳的连续摆动,通过压装齿轮44竖直转动连接于齿轮支架53一侧,压装齿轮44两侧分别竖直固定设置有前齿条支架54和后齿条支架55,升降齿条43沿竖直方向滑动设置于前齿条支架54,压装齿条45沿竖直方向滑动设置于后齿条支架55,转动压杆41与升降齿条43之间设置有升降连杆42,利用转动圆盘38带动转动压杆41沿竖直方向往复进行摆动,转动压杆41能够利用升降连杆42带动升降齿条43进行升降运动,利用压装齿轮44两侧分别与升降齿条43和压装齿条45啮合连接,使得压装齿条45能够与升降齿条43同步相向进行升降运动,利用转动压杆41端部在导杆提升斜面51和导杆下落斜面52的作用下能够实现缓慢摆动提升和快速摆动下落,使得压装齿条45能够实现缓慢下落和快速提升,利用压装齿条45下端水平固定设置有升降压板56,当升降压板56在压装齿条45的带动下缓慢下落的过程中,能够平缓均匀的将工件进行压装加工,避免工件在压装加工过程中产生歪斜误差,提高工件压装加工的质量,当升降压板56在压装齿条45的带动下快速提升的过程中,使得升降压板56能够快速高效的与工件表面脱离,使得压装加工完成的工件能够快速取离,并能继续为下一工件的压装加工做好准备,实现工件的连续高效压装加工,利用压装齿条45下端的升降压板56下侧水平固定设置有压装橡胶层67,确保升降压板56能够平稳的将工件进行压装加工。通过这样的结构,本发明结构设计合理,可以将工件便捷准确的移送至所需的压装工位,并能够将工件平稳高效的进行压装加工,自动化程度高,满足加工使用的需要。By adopting the above technical solution, when a workpiece transferring and pressing device of the present invention is in use, the
本说明书中所描述的以上内容仅仅是对本发明所作的举例说明。本发明所属技术领域的技术人员可以对所描述的具体实施例做各种各样的修改或补充或采用类似的方式替代,只要不偏离本发明说明书的内容或者超越本权利要求书所定义的范围,均应属于本发明的保护范围。The above content described in this specification is merely an illustration of the present invention. Those skilled in the art to which the present invention pertains can make various modifications or additions to the described specific embodiments or substitute in similar manners, as long as they do not deviate from the content of the description of the present invention or go beyond the scope defined by the claims. , should belong to the protection scope of the present invention.
Claims (6)
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201910621494.8A CN110509018B (en) | 2019-07-10 | 2019-07-10 | Workpiece transferring and press-fitting device |
| CN202010319437.7A CN111571162A (en) | 2019-07-10 | 2019-07-10 | Continuous assembling equipment for workpiece machining |
| CN202010319013.0A CN111571161A (en) | 2019-07-10 | 2019-07-10 | Use method of continuous workpiece press-fitting device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201910621494.8A CN110509018B (en) | 2019-07-10 | 2019-07-10 | Workpiece transferring and press-fitting device |
Related Child Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010319013.0A Division CN111571161A (en) | 2019-07-10 | 2019-07-10 | Use method of continuous workpiece press-fitting device |
| CN202010319437.7A Division CN111571162A (en) | 2019-07-10 | 2019-07-10 | Continuous assembling equipment for workpiece machining |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN110509018A CN110509018A (en) | 2019-11-29 |
| CN110509018B true CN110509018B (en) | 2020-06-16 |
Family
ID=68622676
Family Applications (3)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010319437.7A Withdrawn CN111571162A (en) | 2019-07-10 | 2019-07-10 | Continuous assembling equipment for workpiece machining |
| CN202010319013.0A Withdrawn CN111571161A (en) | 2019-07-10 | 2019-07-10 | Use method of continuous workpiece press-fitting device |
| CN201910621494.8A Active CN110509018B (en) | 2019-07-10 | 2019-07-10 | Workpiece transferring and press-fitting device |
Family Applications Before (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010319437.7A Withdrawn CN111571162A (en) | 2019-07-10 | 2019-07-10 | Continuous assembling equipment for workpiece machining |
| CN202010319013.0A Withdrawn CN111571161A (en) | 2019-07-10 | 2019-07-10 | Use method of continuous workpiece press-fitting device |
Country Status (1)
| Country | Link |
|---|---|
| CN (3) | CN111571162A (en) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111230458B (en) * | 2020-03-04 | 2021-08-27 | 苏州知云创宇信息科技有限公司 | Continuous press fitting equipment for tubular workpieces |
| CN112498824B (en) * | 2020-12-10 | 2024-07-09 | 无锡迪渊特科技有限公司 | Rotary lifting translation conveyor belt for FOSB transportation |
| CN116652566B (en) * | 2023-07-19 | 2025-12-26 | 中铁一局集团建筑安装工程有限公司 | A tool for processing prefabricated decoration components |
| CN117226474B (en) * | 2023-10-25 | 2026-03-24 | 芜湖三花制冷配件有限公司 | An automatic mesh expansion machine |
| CN117340580B (en) * | 2023-11-16 | 2025-03-28 | 重庆见龙科技有限公司 | An automatic loading and unloading manipulator for drum brake assembly line |
| CN118648466A (en) * | 2024-07-17 | 2024-09-17 | 临沂农发数字乡村综合服务有限公司 | A planting machine for agricultural management |
| CN118774257B (en) * | 2024-09-10 | 2024-11-22 | 安徽双凤钢结构工程有限公司 | Steel structure net rack connecting piece |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN203956464U (en) * | 2014-07-28 | 2014-11-26 | 青岛力鼎自动化设备有限公司 | A kind of horizontal transfer machine of wheel hub and hub stud press mounting system |
| CN105834712B (en) * | 2016-05-23 | 2018-05-18 | 宁波新邦工具有限公司 | A kind of maincenter feeding station of quick coupling automatic assembling machine |
| CN106975903A (en) * | 2017-04-28 | 2017-07-25 | 襄阳国铁机电股份有限公司 | A kind of motor bearings assembling device |
| CN108455251B (en) * | 2017-12-26 | 2020-06-16 | 湖南创一智能科技有限公司 | Automatic reversing conveying mechanism for workpieces |
| CN208680879U (en) * | 2018-06-22 | 2019-04-02 | 台州创兴自动化设备有限公司 | A kind of water-cooled plate automatic assembling machine |
| CN108705856A (en) * | 2018-06-23 | 2018-10-26 | 徐阳 | A kind of continuous reciprocal eindruckwerk |
| CN108861542A (en) * | 2018-06-23 | 2018-11-23 | 晋正正 | A kind of axle sleeve continuous and perpendicular lifting mechanism |
| CN108581418A (en) * | 2018-06-23 | 2018-09-28 | 屠明州 | A kind of workpiece segmentation press-loading device |
| CN109292377A (en) * | 2018-09-26 | 2019-02-01 | 桐乡市红旗塑料包装袋厂 | A kind of transfer mechanism that continuously back and forth gets stuck |
-
2019
- 2019-07-10 CN CN202010319437.7A patent/CN111571162A/en not_active Withdrawn
- 2019-07-10 CN CN202010319013.0A patent/CN111571161A/en not_active Withdrawn
- 2019-07-10 CN CN201910621494.8A patent/CN110509018B/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| CN111571162A (en) | 2020-08-25 |
| CN110509018A (en) | 2019-11-29 |
| CN111571161A (en) | 2020-08-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110509018A (en) | Workpiece transferring and press-fitting device | |
| CN111300016B (en) | An automatic assembly mechanism for pipe fittings | |
| CN111332743A (en) | Automatic material conveying device for processing tubular workpiece | |
| CN111230458A (en) | Continuous press fitting equipment for tubular workpieces | |
| CN107758221A (en) | A kind of moveable lifting conveyer belt | |
| CN205668788U (en) | A kind of transporter with spinfunction | |
| CN110508949A (en) | Sheet metal processing transport mechanism | |
| CN112777312A (en) | Rapid carrying device for factory automation based on computer application | |
| CN116372538A (en) | Auxiliary clamping tool table for stamping assembly | |
| CN219193382U (en) | Tealeaves cooling conveyer with adjustable | |
| CN219362403U (en) | Jacking transfer device | |
| CN117602333A (en) | A kind of solar cell sheet wire mesh material clamping mechanism | |
| CN214828691U (en) | Plate conveyer | |
| CN116654395A (en) | Flattening and shaping conveyor | |
| KR101728807B1 (en) | Egg Packing Plate Auto Supply Machine | |
| CN108116905A (en) | The case of taking off that automatic mould turnover unloads fruit machine unloads fruit device and method | |
| CN219525103U (en) | A multi-channel right-angle turn roller conveyor | |
| CN114643526A (en) | Rectangular metal shell polishing device and polishing method thereof | |
| CN207671222U (en) | It is connected the mechanism for carrying out convertible transfer to object between assembly line | |
| CN221234537U (en) | Circulation chain type wood chip feeding and storing device | |
| CN207792141U (en) | The case of taking off that automatic mould turnover unloads fruit machine unloads fruit device | |
| CN218878413U (en) | A textile transfer device for a textile production workshop | |
| CN224185080U (en) | Lifting rotary conveyor | |
| CN115043195B (en) | Shoemaking assembly line with independently working tooling plate | |
| CN120270711B (en) | A conveying device suitable for food boxes of different sizes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| TA01 | Transfer of patent application right | ||
| TA01 | Transfer of patent application right |
Effective date of registration: 20200527 Address after: 325000 Meiyuan Village, Sanjiang Street, Yongjia County, Wenzhou City, Zhejiang Province Applicant after: WENZHOU DIANDIANDIAN INDUSTRIAL DESIGN Co.,Ltd. Address before: 314500 Shidai Jiayuan, Xueqian Road, Wutong street, Tongxiang City, Jiaxing City, Zhejiang Province Applicant before: Huang Mingzhu |
|
| TR01 | Transfer of patent right | ||
| TR01 | Transfer of patent right |
Effective date of registration: 20220316 Address after: 130000 Room 101, building 2, No. 539, Zhuoyue East Street, high tech Development Zone, Changchun City, Jilin Province Patentee after: CHANGCHUN ZHONGSHENG TECHNOLOGY CO.,LTD. Address before: 325000 Meiyuan Village, Sanjiang street, Yongjia County, Wenzhou City, Zhejiang Province Patentee before: WENZHOU DIANDIANDIAN INDUSTRIAL DESIGN Co.,Ltd. |
|
| PE01 | Entry into force of the registration of the contract for pledge of patent right | ||
| PE01 | Entry into force of the registration of the contract for pledge of patent right |
Denomination of invention: A workpiece transfer and pressing device Granted publication date: 20200616 Pledgee: Bank of China Limited Changchun Jinyu sub branch Pledgor: CHANGCHUN ZHONGSHENG TECHNOLOGY CO.,LTD. Registration number: Y2024220000089 |